Piezo Fast Tool Servo Ultra‐Precision Micro‐ Machining System With the increasing advancement of science and technology, ultra‐precision processing technology has also been developed rapidly. Microstructure elements with complex surfaces are widely used in many fields such as high‐tech equipment and optical fiber communications. This type of component has a complex structure and high requirements for processing accuracy, and it is difficult to meet processing requirements with traditional processing methods. With the continuous advancement of technology, many ultra‐precision machining methods have emerged that can process microstructured surfaces that meet the needs, such as photolithography, micro‐ grinding, laser processing, and fast tool servos. These methods have their own advantages and disadvantages. Among them, the fast tool servo is a relatively classic ultra‐precision machining technology, and it is one of the hotspots in the research of micro‐structure turning.
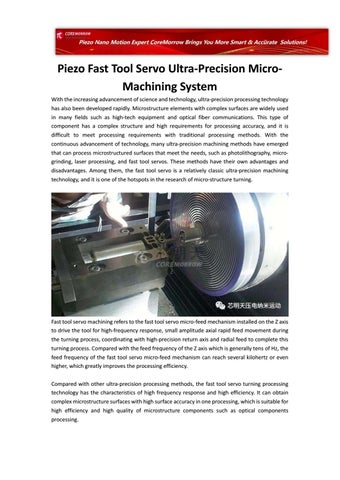
Fast tool servo machining refers to the fast tool servo micro‐feed mechanism installed on the Z axis to drive the tool for high‐frequency response, small amplitude axial rapid feed movement during the turning process, coordinating with high‐precision return axis and radial feed to complete this turning process. Compared with the feed frequency of the Z axis which is generally tens of Hz, the feed frequency of the fast tool servo micro‐feed mechanism can reach several kilohertz or even higher, which greatly improves the processing efficiency. Compared with other ultra‐precision processing methods, the fast tool servo turning processing technology has the characteristics of high frequency response and high efficiency. It can obtain complex microstructure surfaces with high surface accuracy in one processing, which is suitable for high efficiency and high quality of microstructure components such as optical components processing.
Fast tool servo turning processing requires high‐frequency response and high‐precision micro‐feed. At present, the driving mode of the micro‐feed mechanism is mainly driven by piezoelectric ceramics. The fast tool servo driven by piezoelectric ceramics has many advantages such as fast response speed, high acceleration, wide frequency response range, and easy control. The fast‐tool servo micro‐feed mechanism is a very important component in the fast‐tool servo processing system. As a high‐speed and high‐precision displacement output mechanism, its performance has a direct impact on the surface quality of the micro‐structure processed by the fast‐tool servo processing. The P92 and P93 series piezoelectric fast tool positioners designed and developed by CoreMorrow have the advantages of large bearing capacity, fast response speed, wide frequency range, and nanometer precision. They are the first choice for fast tool servos. Coremorrow Piezoelectric Fast Tool Positioner CoreMorrow has nearly 20 kinds of fast tool positioning stages specially designed for fast tool servo micromachining. They have differences in performance such as displacement, frequency, closed loop mode, output, driving voltage, appearance and structure. In terms of displacement parameters, the working frequency is different under different displacements from ten micrometers to more than one hundred micrometers. For example, CoreMorrow P92.X20S fast tool positioning stage, under 18μm stroke, the working frequency can reach 95Hz; under 9μm stroke, the working frequency can reach 190Hz; and under 1μm stroke, the working frequency can reach 600Hz. There are a variety of closed‐loop options for piezoelectric fast tool positioning stage, such as capacitive, inductive, and strain‐type closed loops, and external closed‐loop control methods can also be used. The different closed‐loop methods affect factors such as the control accuracy,
operating frequency and cost of the fast tool positioning stage. P92.X20 Series Fast Tool Positioning Stage
Stroke for the above: 18μm Drive voltage: 0~150V Carrying capacity: 300g Closed loop : optional P92.X25 Series Fast Tool Positioning Stage
Stroke: 23μm No‐load harmonic frequency: 3000Hz Output: 1000N Closed loop: optional
P92.X40 Series Fast Tool Positioning Stage
Stroke: 40μm Drive voltage: 0~1000V Output: 3000N Custom cooling holes P92.X70 Series Fast Tool Positioning Stage
Stroke: 75μm Positioning accuracy: 0.01%F.S. Customized dust‐proof and drop‐proof type Closed loop: optional P93.X70 Series
Fast Tool Positioning Stage
Stroke: 81μm Carrying capacity: 20kg Resolution: up to 3nm Closed loop: optional Coremorrow Fast Tool Positioning Stage Applications
Light Guide Plate Processing
Turning Of Optical Components
P93 Fast Tool Stage and Manual Adjustment Stage Combined with Ultra‐Precision Machining
Fast Tool Positioning Stage with Customized Heat Dissipation Device