FROM THE CARRIAGE AGE.........
TO THE SPACE AGE.......
The Birth and Growth of the Concrete Masonry Industry
By Joseph Bell and Contributors
Published by The National Concrete Masonry Association
Copyright by National Concrete Masonry Association 1969 All Rights Reserved
Printed in the United States ~ Library of Congress Catalog Card number 78-113382
1
TABLE OF CONTENTS
I The Beginnings…. 1
II Francis J. Straub 10
III The Golden Decade 16
IV Gallery of Early Concrete Masonry Buildings 30
V Depression 32
VI The Rebirth of The National Concrete Masonry Association 46
VII War and Post War 52
VIII The Space Age 67
IX Gallery of NCMA Presidents 82
X Lightweight Aggregates 87
XI Atmospheric or Low Pressure Curing of Concrete Block 94
XII Autoclave Curing 107
XIII The Transportation and Handling of Concrete Block 117
XIV The Evolution of Concrete Masonry Machinery 124
XV Development of Specifications for the Concrete Block Industry 136
XVI Gallery of Modern Concrete Masonry Buildings 142
XVII But Not Endings .... 145
2
The Beginnings . . . . .
Only a few decades after Americans had won their independence from England, a pair of enterprising masons named Foster and Van Derburgh, cast about for a way of making a precast building block larger than the clay brick then prevalent. After a good deal of experimentation, they discovered that powdered quick lime and moist sand could be mixed together and molded by pressure into a usable building block, providing the end product was subjected to a steam treatment to hasten the slaking action. The natural mechanical heat thus generated formed a silicate of lime which turned out to be Foster and Van Derburgh's cement, holding their building blocks together.
By modern standards, Foster and Van Derburgh had some serious shortcomings in their product. The blocks were solid, made entirely by hand in awkward wooden molds, oversized, very heavy, and exceedingly hard to handle. They also, technically, weren't concrete blocks at all, since the sand-lime mixture wouldn't qualify today as a cementing agent for concrete now defined as a mixture of cement, water and inert materials, placed in a plastic condition but hardening quickly as a result of the hydration of the cement. Saddled with these shortcomings, the pioneering building blocks of Foster and Van Derburgh although patented in the early 19th century never caught on.
Instead, the evolution of concrete block moved to England, where experiments with a solid concrete block some quite successful had been taking place since the turn of the 19th century. The first recorded system was developed by a Brighton builder named Ranger, who patented a concrete block in 1832. Ranger made his concrete by mixing aggregate of sea gravel, broken flints, masons' chippings and similarly exotic inert materials with powdered lime and boiling water. Mixing only enough to fill a single mold, Ranger would ram the material into the mold to drive out the air. The boiling water made the concrete set so rapidly that within ten minutes Ranger could remove the sides and end of the mold, leaving only the bottom to support the block, which were allowed to cure for about two weeks. Ranger used his block for a group of houses in Pall Mall and the walls of the College of Surgeons, which were perfectly sound when the building was altered fifty years after Ranger built it. In spite of its successful application, however, the system apparently died with Ranger.
The next recorded experimentation with concrete block is found in a British patent granted Joseph Gibbs in 1850. The Gibbs patent described a method of building solid concrete walls by means of timber forms or lattices on either side. Also included in the patent was the specification that block could be hollow cast, with the hollows to be filled with concrete, after each course. However, in practice this was not always done, so the Gibbs patent was actually the beginning of both the monolithic wall and the hollow concrete building block.
1 I
In 1865, a Mr. Tall patented an apparatus to form a trough in which concrete could be deposited at the job site, but a company formed to work Tall's patent quickly disappeared. The same fate was shared by a number of other appliances of similar design, usually abandoned because they couldn't meet such essential building requirements of the day as adaptability to different varieties of plans, simplicity, ease of maintenance, economy and durability. The disadvantages of requiring a jobsite apparatus or sizable amount of rough timber to make the molds for depositing concrete were simply overwhelming. Stucco was also needed to cover up the rough appearance of the concrete. Consequently, inventors in the late 1800s turned their attention to casting hollow or solid concrete block that could be laid up into a wall. There were several important advantages of the "block" system over the monolithic wall. Unskilled labor, even women and boys could be employed. The block could be made whenever it was convenient and then stored in the yard as long as desired. Workers employed on a seasonal basis elsewhere could be hired to make block, and builders regarded the lag between manufacture of the block and their shipment as an opportunity to detect inferior quality products.
As soon as these early pioneers discovered that hollow block could be produced with satisfactory strength and durability, the solid block virtually disappeared. The problems in handling solid block from the plant to the job and in the actual construction work were insurmountable. The laying of concrete block in a wall required skilled and therefore expensive labor, and the workmen simply would not handle the heavy, unwieldy solid block. In addition, when the block were made of hard materials, they couldn't be sawed smaller as could stone.
And so, very early in the history of concrete block, the people developing it were forced to look away completely from the solid to the hollow block. In 1866, a U.S. patent was granted to C. S. Hutchinson on a hollow building block Lind wall with continuous vertical air spaces. Two years later, Thomas J. Lowry was granted a patent on a similar hollow block wall and, in 1874, T. B. Rhodes patented several different forms of hollow building block of "concrete or other material which in its plastic condition may be molded into the required form." Since no method of molding the block was suggested, it would seem that the patent granted Rhodes the exclusive right to manufacture the block he described by any method of molding then known.
In an effort to escape the cost of transporting and difficulty in handling concrete blocks, slabs of thin plates of concrete were developed to form a mold to hold the concrete (similar to the apparatus of rough timber once used). This system also eliminated the application of any surface finish. One of the most ingenious block of this type was introduced by J. J. Lish of Newcastle, England, in 1878. Units of his concrete facing slab, called a “Z” block, interlocked, and it was claimed that a strong wall could be built without filling the cavities with concrete. Lish's block were made in wooden or iron molds, where the concrete was allowed to harden for 24 to 48 hours before the mold was removed. This was a tedious process that also proved too costly for commercial success.
2
Harmon S. Palmer is generally credited with the development of the first commercial process for the manufacture of concrete block in the United States. After ten years of experimentation, Palmer patented the basic principle of the hollow concrete building block machine with removable cores and adjustable sides in 1900. The Palmer hollow concrete block used in a home in 1897 were 30 x 8 x 10", made on the job of Portland cement and sand to save the cost of transportation and eliminate breakage in handling during loading and unloading. Palmer's block were tongue-and-groove. with interlocking joints and recessions for the installation of doors and window sash. They were also so large and heavy they had to be set in the wall with the aid of a hand cranked derrick
During the next several years, there appeared on the market a number of block machines, all of the handtamp variety, but with some minor variations. (See Chapter XIV for a detailed discussion of block machines.) An intense competition between machine manufacturers developed, including the licensing of exclusive territories. There was a scramble to set up concrete block plants all over the country, and a series of suits and counter suits involving the Palmer patent clogged the courts.
While the block machinery manufacturers were fighting their legal infringement battles, they were also enticing customers with claims like these (in 1904):
“You can build your own house with machines and save money even if you throw the molds away afterwards.”
“Pettyjohn's hollow concrete block machine was used for this job as it would have been impossible with any other machine.”
“If rival interests don't like to hear about our machines putting up so many buildings the only way they can stop the machines is to purchase them.”
One machinery manufacturer took a full page ad to warn buyers: "Don't be deceived into buying a machine just because it makes a hole in a block. BEWARE of charlatans who know nothing of the business but want the public's money on other's success."
This was the era of the hand tamp machine, when a three-man crew could turn out 200 block in a 10-hour day. Block machines had collapsible mold sides to facilitate removing the 8 x 24-in. units, and the manufacturing process was a laborious, back-breaking job. But the ads were enticing and the potential profit very real, and these facts attracted hundreds of novices into the concrete block business. It was a spectacular though decidedly disorderly beginning of an industry.
3
Markets for the new product were sprouting daily from a construction soil made fertile by the high cost and scarcity of competing materials. New homes were in great demand, and lumber prices in 1906 were 64 percent and common brick 59 per cent above the 1898 prices. It was only natural, that builders should look around for some substitute for these materials. And since one concrete block in 1906 replaced 28 common brick, it was also natural that builders would turn to this new material as a partial solution to their problems. Consequently, for the next few years, builders purchased all the concrete block that this blooming industry could supply.
Things were looking up for block on other fronts, as well. For example, in 1905, the United States government adopted concrete block for hospitals, warehouses and barracks in the Panama Canal Zone and the Philippine Islands. Before adopting this new product, the government subjected it to thorough and rigid tests. Palmer then agreed to send his own men to Panama and the Philippines to supervise the manufacture of the block.
Domestic concrete block manufacturers had several cost advantages over competing materials. Freight charges on lumber, stone, and usually on brick were greater than block, which was locally manufactured and used materials (except cement) that were readily available.
At the same time, the development of the Portland cement industry which began in 1900 continued at a rapid rate, making cement quickly and easily available.
Cement could be obtained at reasonable prices which declined 16.5 percent between 1900 and 1906 and could be purchased in small quantities. Thus, the growth of the concrete industry closely paralleled that of the portland cement industry during the first few years following 1900.
In response to this low cost of raw materials and burgeoning demand for the product, there was a tremendous influx of producers into the concrete block industry in the early 1900s. Farmers, clerks, men from all walks of life rushed into the business, all expecting to become rich overnight. No skill, knowledge, ability or financial strength was necessary to get into the business (although the lack of these qualities got a lot of people out rather quickly). All that was needed to start a concrete block plant was the price of the machine, at that time about $125.00. Many producers made their block outside or in a shed, hence the origin of the term "backyard" or "woodshed" producer, which still hangs on today.
There were some long-lasting success stories that date back to this period. In Omaha, Nebraska, for example, Nels J. Peterson took a leave of absence from the Union Pacific Railroad to mine limestone. He was impressed one day with some rock-faced concrete he saw on a building site, and weeks later, laboring in a quarry hewing stone, he couldn't get that block out of his mind. (Later, on his death bed, he was to
4
recall for his son, Earl: "When I saw that block, I really saw something.") "Why," he asked himself, "should I hew these stones when I could make them in a mold?" So he took his wife's $800 inheritance and invested it in a block business that has grown and prospered for well over half a century.
A lot of other men like Nels Peterson were doing the same thing, although they didn't all turn out to be as successful. One who did was a young man named Jesse Besser, then working in his father's cement plant in Alpena, Michigan. He, too, was impressed by the pioneering efforts at concrete block and remembers that he "saw a mass market, even then, although I had no understanding of its dimensions." While Nels Peterson was making block ("Terrible block," his son remembers, “with pit run sand, unwashed, dumped on a floor and hoed, watered and batched, so heavy on cement a bag made only ten blocks that it lasted forever.”), Besser was making block machines. The block in those early days sold for the same price it is bringing 70 years later, but the block machine, likely to cost $100,000 in 1970, sold for $100 in 1906.
Not all newcomers to the concrete block industry were as skillful or as competent as Nels Peterson and Jesse Besser. A business paper of the day noted: "With the flood came many incompetents, and with the flood also there rose, like mushrooms in the night, a rush of manufacturers whose strongest desire was, in many cases to get a piece of the good thing that was going around, regardless of the past, present or future of the business."
A. L. Johnson, who joined the Ideal Cement Stone Company in 1913, remembers these very early days: "Mixing the concrete was a laborious, time consuming operation. The sand aggregate was unloaded by hand into a stockpile from which it was taken in a wheelbarrow and dumped into the mixer, along with cement from cloth sacks. After a minute or so of dry mixing, water was added. The batch was mixed another five minutes, then dumped at the side of the block machine operator who scooped the not-too-wet concrete into the block machine and started tamping to make one block at a time. In those early days, the mixer man and the block machine operator were paid 25¢ per hour and worked a ten hour day. The average output was 250 to 300 standard blocks per day, and the yield per sack of cement was 12 plain unfaced blocks and 10 of the rock faced blocks, a "must" in those days."
George Saffert, a Minnesotan and another industry pioneer, remembers buying his first hand-tamping block machine for $68 in 1910, and his second from Sears, Roebuck for $87. It included a cast iron pallet formed with a good hand grip projecting on each end. "Our average production on the first machine was nine blocks per man hour. With the Sears machine it was 10 blocks per man hour, including stock piling. Occasionally we moved the equipment to the building site and made the blocks on the spot to save transportation costs, and also do jobs beyond the reach of the horse and wagon delivery of that era."
5
Most block makers knew little about their real costs of production. If, at the end of the week, there was not sufficient cash on hand to pay the workers, the shortage was made up by reducing the amount of cement and labor going into each block. One of the leading block makers of the period confided that he was finally making money by producing a block just good enough to hold together until it was delivered to the job. This inefficiency, lack of knowledge, and in many instances deliberate production of an inferior product soon ruined the business for poor producers. Unhappily, it dragged down many of their more honest and efficient competitors, as well.
The embryo block industry was having plenty of trouble in other directions, too. Although the Bricklayers and Masons International Union had opposed concrete block from the beginning, the president of the union made a nationwide tour in 1902 in an effort to unionize concrete workers on the theory that if the concrete block industry could not be destroyed, the only remaining approach was to get the new industry into the fold. But the bricklayers' prejudice against concrete block was not easily put down. An anguished block producer said in 1906: "I have seen many jobs completed which were very unsightly because of carelessness of the mason in allowing the blocks to be spattered with mortar. This can easily be avoided and in most cases it comes from masons who are prejudiced against the use of concrete block." This complaint was not unusual, often concrete block were simply thrown together, not laid true or level. The bricklayers principal complaint against concrete block was its weight. They could hardly be blamed, since 12 x 9x 32" block weighed 180 pounds. The bricklayers were also fearful that concrete block would take away their livelihood since one block was equal in size to 28 bricks.
To deal with these and a good many other problems besetting the new industry, concrete block producers began to take collective action shortly after the turn of the century. The National Association of Cement Users was organized in 1905 for the purpose of "disseminating information and experience upon and to promote best methods to be employed in various uses of cement by means of conventions, reading, and discussions of papers upon materials of a cement nature . . . the exhibition and study of materials, machinery, and methods and to circulate among its members by means of publishing the information thus obtained."
The first national industry convention was held in Indianapolis in 1905, and the first machinery show took place a year later in Milwaukee, sponsored by the Concrete Block Machine Manufacturers Association which was organized in 1905 to "improve the quality of concrete block."
Appropriately enough, a man named O. U. Miracle addressing the Block Machine Manufacturers Association convention at Ames, Iowa, in 1905 presented the first recorded paper on improving the quality of concrete block, emphasizing that one inferior concrete masonry job would offset many good jobs. He pursued the argument made repeatedly in later years that concrete block must have the complete confidence of architect, builder, legislator, insurance companies, and the general public if it were to prosper.
6
Miracle was a few years ahead of his time when he suggested approaching the Underwriters' Laboratory to conduct tests on concrete block and develop recommended specifications for the concrete block plants to meet in order to market a product bearing the stamp of approval of the insurance companies.
By 1905, an estimated 1,500 companies in the U.S. were manufacturing concrete blocks a product virtually unknown just five years earlier. In light of such a chaotic development, it was hardly surprising in spite of O. U. Miracle's exhortations that quality suffered and strong prejudice developed among architects, builders and the general public toward concrete block during its first decade of growth. This reaction to block, plus a construction recession and ample supplies of competing materials by 1910 cut the ground temporarily from beneath the new industry.
Up to this time, even Nature had seemed to be cooperating with concrete block. In the embers of San Francisco, after the earthquake and fire of 1906 destroyed almost two-thirds of the city, two sizeable concrete block buildings a church and a factory stood virtually unharmed. About the same time, the three core unit later to make up some 90 per cent of all block produced was developed. By providing a much lighter unit with the same load-carrying capacity, it destroyed much of the weight argument against concrete block.
But these positive indicators weren't nearly enough to overcome the generally inferior quality of concrete block, at first overlooked because of the great demand for building materials and the shortage of brick and lumber. By 1910, the brick industry had plenty of excess capacity, the lumber supply was sufficient again, and prices of both products were reduced. With no shortage to protect it, concrete block could not compete with other building materials on anything like price equality.
At the same time, the block industry was suffering many other types of malaise. Since most producers were small, there was virtually no trained management. Shoestring operators couldn't finance inventories of block, so curing was inadequate. Shortage of working capital caused producers to cut down on cement and thus reduce quality even further. In appearance, most block resembled the cheapest type of quarry stone and was therefore consigned mostly to foundations and basements. (The introduction of ashlar block in various textures, colors and patterns in 1912 helped break away from rock-face block.) Fire insurance rates for block were also high because of its structural weakness, and there was very little consistent advertising or sales promotion effort in the industry. Even the quality manufacturers generally made their block, then waited for someone to come and buy. (The clay brick industry, by contrast, was building a quality image with widespread, sustained advertising.)
As a result of these factors, many of the marginal operators, attracted to concrete block by the promise of a quick and painless profit, began to drop out of the business. The survivors, aided by increasingly sophisticated block machinery, more efficient plant operation and better means of delivery, began to carve a permanent, substantial place for the industry in the building construction field.
7
By 1914 production had increased three fold over the 1901 figure. The block producer in those pre-World War I days was able to turn out about 1,800 units per day with the same three-man crews. This same period saw the introduction of the semi-automatic down face machine, a unit that featured more automatic operation than the block industry had seen before. But a block machine could still only turn out one block at a time when the first gasoline trucks hand cranked, cantankerous, with heavy hardwood steering wheels, began to replace the horse-drawn carriage in transporting concrete block from factory to job.
Probably the most far-reaching development of this volatile period came near it's end from the fertile mind and wit of a Pennsylvania bricklayer named Francis J. Straub, the first man to bring showmanship and imagination to an industry that was fast building an image of dullness, ugliness and inconsistency.
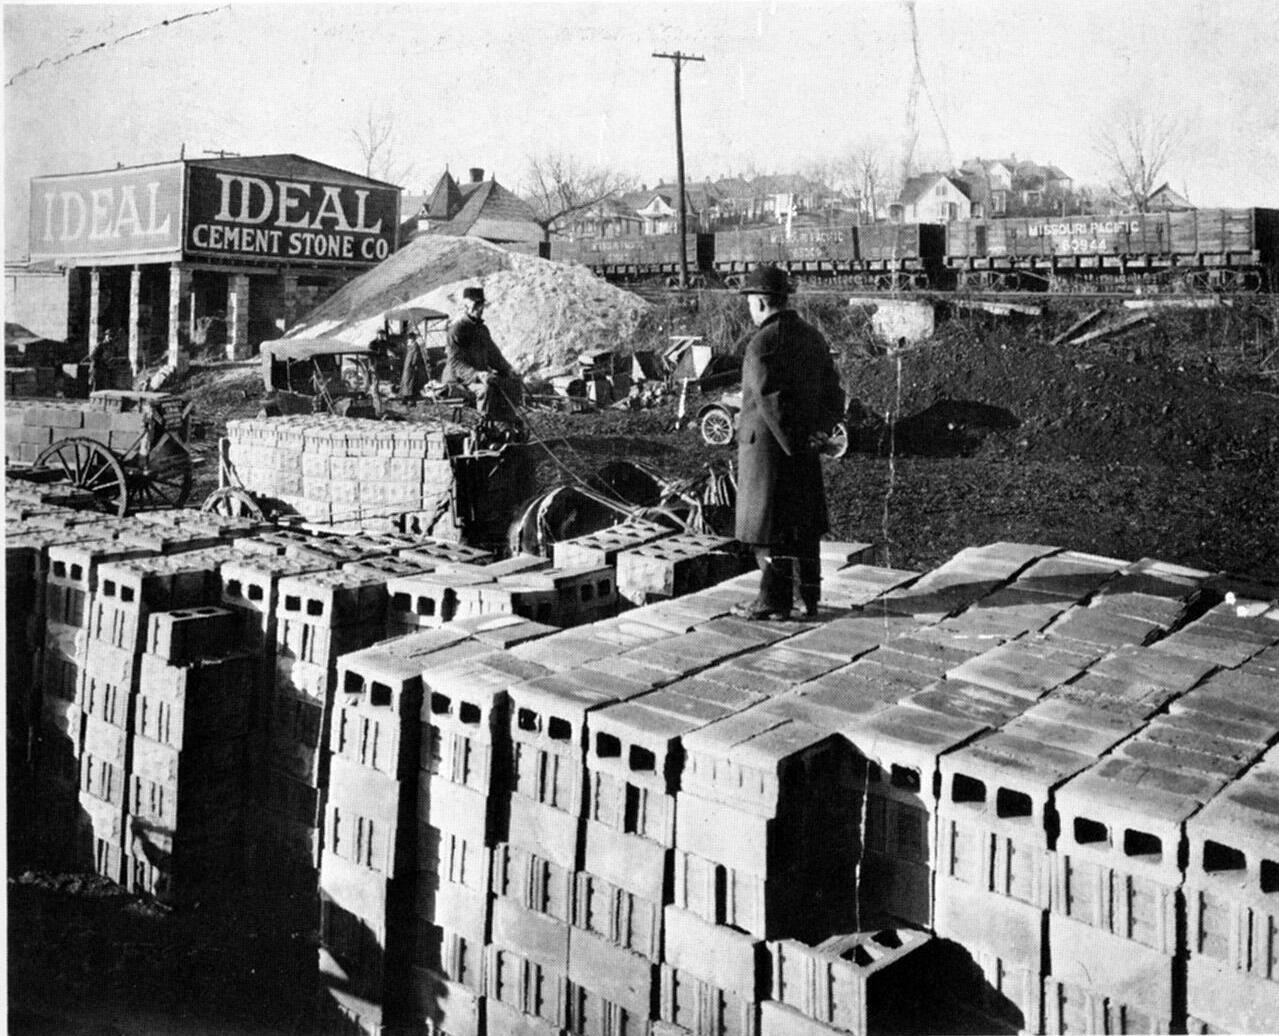
This is how an early concrete block plant looked. Nels J. Peterson, founder of Ideal Cement Stone Co. of Omaha, Nebraska surveys his storage yard in 1913. Note horse-and-wagon transport and the freight cars awaiting loads of block on the nearby siding.
8
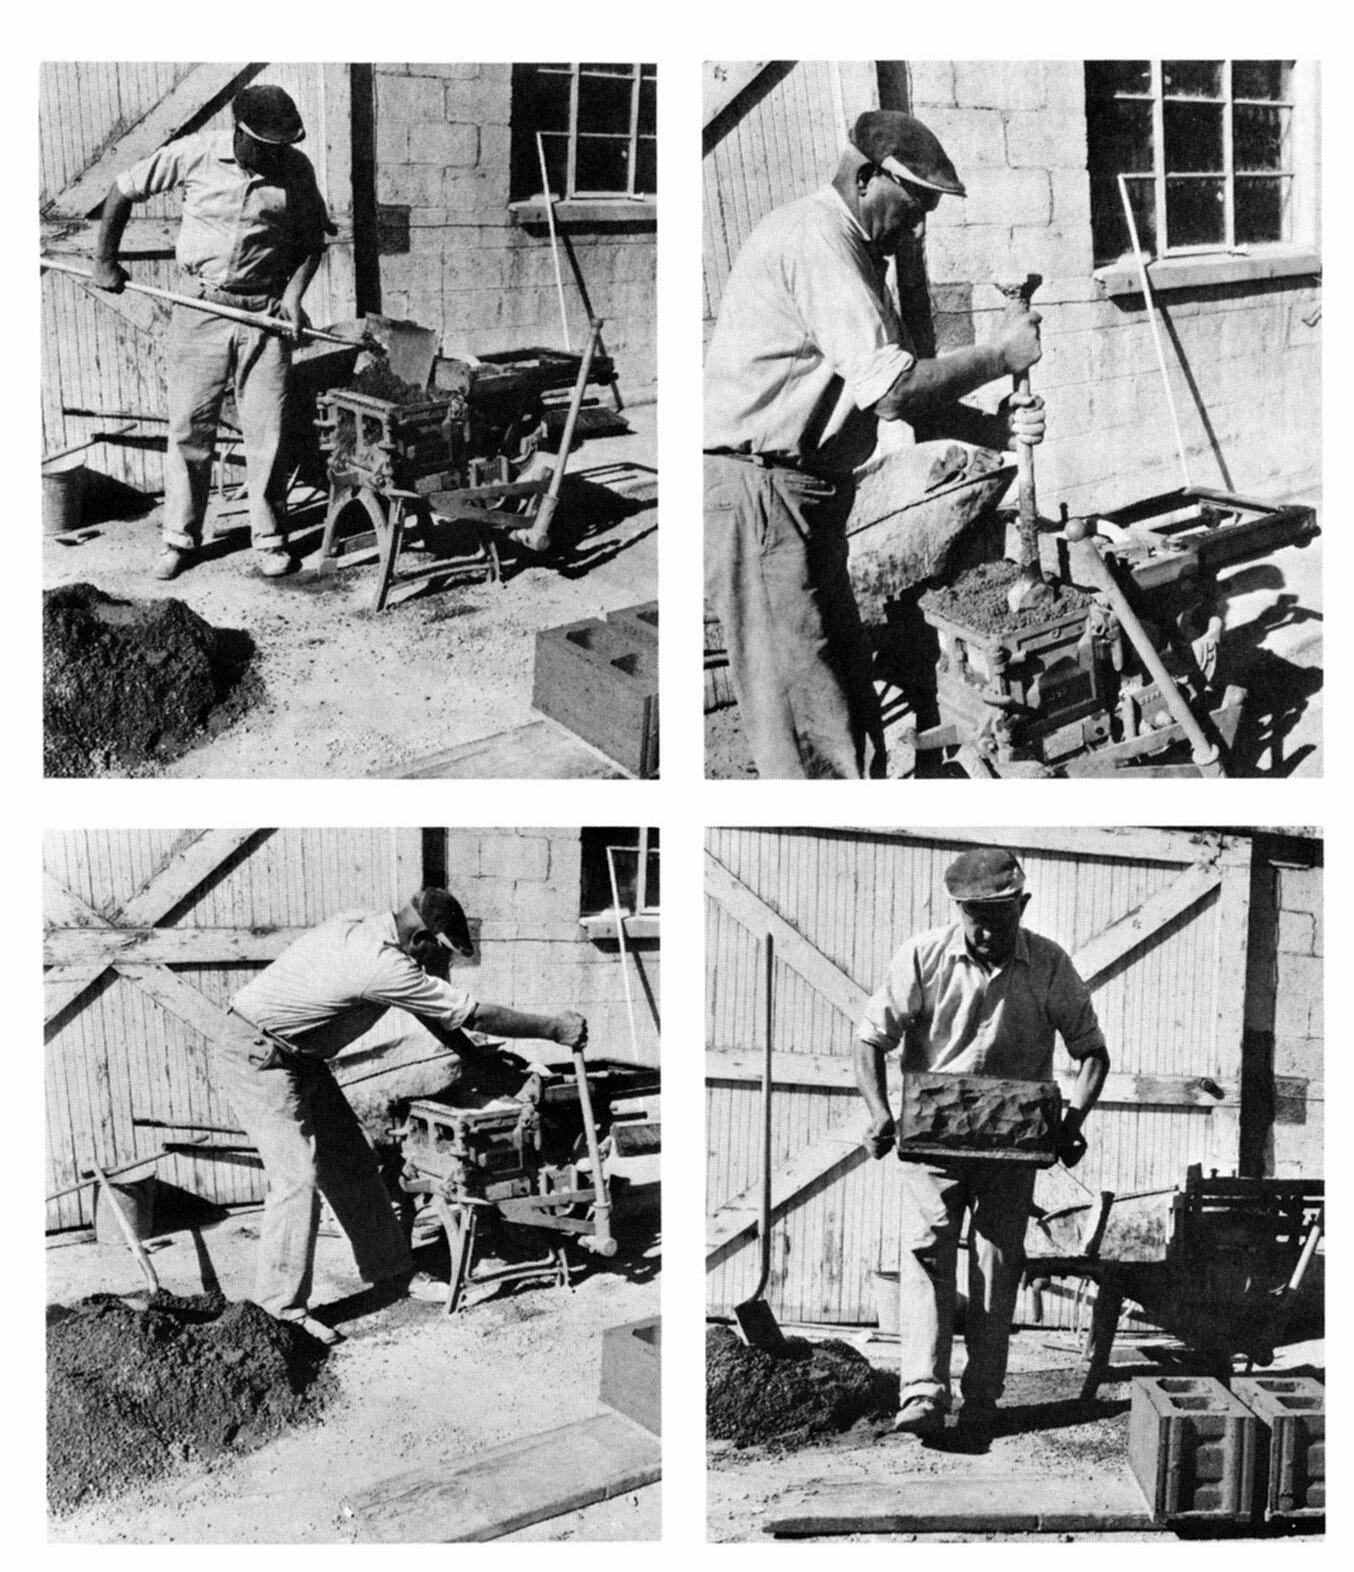
This is how concrete block was made in the very early days and for a good many years thereafter in backyards and basements. Pictured here is the process involved in turning out one concrete block on a model of the early hand-tamp machines. In (1) the workman fills the machine with cement and aggregate, hand mixed on the ground. In (2) he hand tamps the mixture, in (3) discharges the finished block and in (4) carries it to a crude pallet for curing.
9
Francis J. Straub
The first known tests on cinder aggregate for concrete block were conducted by Prof. Ira H. Woolson at Columbia University in 1909, the same year cinderblock were approved for use in the borough of the Bronx. (Three years later, they were approved for all the New York boroughs.)
Other pioneers experimenting with lightweight aggregates during this period included Englishman W. J. Steward (issued a British patent in 1917 for an aggregate made from burned clay), C. E. Barglelaugh an American patent the same year for a ground lava rock aggregate), and Stephen Hayde who in 1918 was granted a patent "covering the preparation of materials suitable for use in the manufacture of molded articles." Hayde's materials were clay and shale that turned into bloated clay balls when burned at high temperatures. The resultant clinkers which became widely known as Haydite when crushed, were very light and first came into use as a concrete aggregate for ships during World War 1. The war ended before many ships were built, but the aggregate had been launched for a long and useful career.
Although all of these people and events were decidedly important in the evolution of the concrete masonry industry, they were dwarfed by the work and the personality of an eccentric and individualistic Pennsylvania bricklayer named Francis J. Straub, the inventor of cinderblock. When Straub came along, the concrete masonry industry was lacking more than anything else imagination. Straub supplied it in copious quantities.
It has been claimed that several other plants produced cinderblock between 1910 and 1912, but little progress was made in the use of cinders in the manufacture of concrete block until F. J. Straub of New Kensington. Pa. began production in 1913. Francis Straub was a very good bricklayer who studied and experimented for many years with steam boiler cinders as an aggregate for concrete block. His purpose was to make block cheaper by using this waste material and at the same time produce a block that was lighter and nailable. Straub, himself, described this cinder concrete building block as "made from the entire ash or cinders fromthe combustion of either hard or soft coal, the large particles crushed to a point that will permit passage through a one-half-inch mesh screen. The intention in the manufacture of cinder concrete block is to produce a block of ample strength for all building requirements for either a bearing or non-bearing wall, and of sufficient porosity to provide the other essential characteristics of this cinder concrete block, namely, nailability, heat insulation, light weight. It is found that this is most readily accomplished by a mixture of about one part of cement to six parts of cinders. The strength of the block is specified at 800 lbs at 28 days age. The density and the
10 II
strength of the block can be greatly increased either by increasing the amount of cement or by changing the proportions of coarse and fine material in the aggregate."
Engineers and architects were perhaps understandably slow in light of the chaotic condition of the concrete block industry at that time to accept the new Straub product as a satisfactory building material. In many cases, it met with open ridicule a fact the inventor liked to recall with glee in later years but Straub persisted and built a number of houses and commercial buildings in his home area with his new product. He first applied for a U.S. patent covering his process on Nov. 9, 1915. It was refused. Straub finally convinced the patent office that he had something new in proposing that the complete residue of the fuel after burning the whole cinder should be used, and he was accordingly granted a patent on Jan. 16, 1917.
Straub's patent provided that "the ground mixture of cinders retains all of the usual accompanying adhering portions of the cinders in the resulting product, and it is essential that the original mass of cinder ashes as it comes from the furnace, grate bard, or other source remains in the resulting mixture without separation or change in proportion." It was further provided specifically that no sand or other aggregate should be added to the cinders. The greatest advantage of cinderblock, was, of course, its lighter weight. A standard 8 x 8 x 16" cinder block weighed 20 pounds less than a comparable sand and stone or gravel block. Much of the resistance of the masons and bricklayers to laying concrete block was thus eliminated by this lighter block.
Straub struggled during those early years to establish a few plants operating under his patent, the largest at Lancaster, Pa., where cinderblock was used for many buildings, ranging from garages and factories to school houses, banks, hospitals and churches, all with perfect success and much satisfaction to the owners.
Their use elsewhere, however, in the period 1915-1922 was relatively limited. By 1922, only about a dozen cinderblock plants had been licensed, all in the East and mostly in Pennsylvania. Only 25,000 cinderblock were made in 1919 (by 1926 there were 70 million being made!), but the promise was there and it had been spotted by some of Straub's competitors. One of them needing to hype his business began manufacturing a concrete building, product made from cinders and cement, with the addition of a fixed percentage of sand. Since the Straub patent specifically provided that no sand be used, the competitor apparently thought he was protecting himself legally. Straub started infringement proceedings and lost in a lower court. He appealed to the U.S. Circuit Court of Appeals and a unanimous decision was handed down on July 3, 1919, reversing the lower court and fully establishing the validity of Straub's patent. In the opinion of the appellate court, the fact that a nail could be driven into the block fixed the guilt definitely on the infringers. The court was primarily concerned with the qualities of the finished product, a precedent that would serve Straub well in the years ahead.
11
From this time on, Straub's procedure with poachers on his cinder block domain was routine. He would arrive in town, hire a taxi, visit the poacher's plant, buy a half-dozen concrete block, take them to a local court where he would triumphantly drive a nail into them and then file a complaint against the errant block producer. Thus the Court of Appeals decision greatly strengthened Straub's competitive position.
So did a merger with the Brooklyn Crozite Brick Corporation in April, 1922. Brooklyn Crozite Brick was a manufacturer of concrete brick with a large plant located in the geographical center of the borough of Brooklyn. While this product had been widely distributed, it was not a commercial success. E. B. Cadwell and Company had made a substantial investment in Crozite and had taken over its management to try and rehabilitate the business.
Cadwell was impressed with Straub and organized a new corporation known as Crozier-Straub. Inc., to which were transferred the patents owned by Crozier on machinery and processes for manufacturing concrete products and the cinderblock patent of Straub. The marriage was an immediate success. Less than a year later, Crozier-Straub, Inc. had 50 licenses many of them in the midwest and beyond with a production capacity of 40 million cinderblock per year.
The Straub licensees formed the National Cinder Concrete Products Association, with F. J. Straub himself, as president, for the stated purpose of cooperative research and promotion. It was also undoubtedly formed for mutual protection. While he was not entirely successful, Straub tried very hard to maintain the quality of his licensees' products. He fully realized that one plant producing an inferior cinderblock would bring discredit upon the entire group. Accordingly, he tried to insure a minimum compressive strength of 750 pounds per square inch of gross area, for all cinder block.
When Straub's product was first introduced and before sufficient information was available regarding its characteristics there was considerable hesitation on the part of engineers and building inspectors in permitting its use. But by 1923, after ten years of experience with the product, cinderblock was being adopted in many city building codes. A vital factor in this acceptance was a long series of tests in the early 1920s.
For two years, Straub cinderblock were pounded, pummeled, burned, hosed and subjected to every known building test and passed them all. The Underwriters Laboratory (1922), the Structural Materials Laboratory of the Lewis Institute (1923), Rutgers University (1923), the Pittsburgh Test Laboratories and Columbia University (1924) all ran extensive strength tests on cinderblock after subjecting it to all sorts of punishment. All of these tests indicated that the strength of the cinderblock could be easily maintained at 700 psi at 30 days (the average recommended by the U.S. Dept. of Commerce for masonry walls at that time) and that the strength of the block increased perceptibly, at least up to six months.
12
Extensive fire tests indicated the cinderblock was absolutely firesafe. The Fire Underwriters Laboratory conducted numerous tests of its own and observed tests at Lancaster and Reading, Pa. Results indicated almost total fire resistance with very little loss in strength for the block walls. The Reading test was typical. A test house was built of sample panels of cinderblock, brick and hollow tile, subjected to a raging fire for more than an hour, then doused with water under pressure. Only two of the 637 cinderblock showed any damage, while almost all of the tile and brick were cracked and unfit for use.
Similar positive results emerged from frost and moisture tests. Although well within the absorption limits set by the U.S. Dept. of Commerce, cinderblock contained large internal air spaces. Because there was practically no capillary action, producing what is ordinarily known as suction in the clay products, there was also no tendency for moisture to be drawn through from a wet exterior cinderblock surface to the inside wall surface. Therefore, from the standpoint both of durability of the block against freezing when wet and the damp-proofness of the cinder block wall, the absorption recommendations commonly applied to other forms of concrete block did not necessarily apply to the cinderblock.
A typical series of freeze-thaw tests took place at Columbia University in 1924. In these tests, the saturated blocks were frozen, thawed, and resaturated twenty times. The strength of the blocks after repeated freezing and thawing cycles was in some cases, greater, in other cases, less, than the strength of similar blocks before freezing, from which researchers concluded that freezing and thawing had no particular effect upon the strength of these blocks.
Additional tests proved the high insulation qualities and soundproofness of cinderblock walls. The block could also be cut easily to a straight line and channeled for conduits and pipe. Nails could be driven into the block, and these nails would hold. And the rough surface texture of the cinderblock made a perfect base for the application of interior plaster and exterior stucco. Cinderblock was sold at about the same price as competing products, but the savings due to the ease of laying made cinderblock walls from 20 to 35 per cent less costly than brick.
Straub's particular genius transcended these impressive test results however. He not only subjected his block to extensive testing, but he merchandised the results an element heretofore sadly missing in the concrete block industry.
For example, when a Straub licensee in Pennsylvania needed a new plant, it was built of Straub cinderblock, with one exterior face of the building used as a sample panel to demonstrate the application of stucco. The building also used a variety of Straub block, thus functioning as a salesroom as well as a manufacturing plant. When Straub put up a model home to demonstrate the possibilities of cinderblock he told a reporter, straightface, that the cost of the dwelling was so low that he was afraid to tell the truth
13
because he was certain that his word would be doubted. When a devastating fire raged through a commercial garage in Kingston, Pa. destroying 100 cars Straub got a letter from the fire chief attesting that "the only walls remaining intact were those built of Straub cinderblock, and I noticed particularly that none of the block or mortar joints bonding them were even fractured." He induced the Chief Engineer of the city of Pittsburgh to attend a fire test in Reading, then got him to write a letter to Straub saying, in part, "For more than four years I have been convinced that Straub blocks are paramount in fireproof qualities compared with any other known building material."
He solicited and surprisingly, even in a far less complicated age received endorsement letters from a wide variety of architects, engineers and builders. Typical is a solicited letter from Pittsburgh architect Carlton Strong, saying: "In reply to your inquiry for my opinion of the value of Straub Cinder Blocks in building construction, I beg to say, after considerable experience with them, that I have the highest opinion of their many structural properties."
All of this made highly digestible promotional fodder to Straub, who bundled it flamboyantly and fed it to the building trade in a distributional arc that grew steadily each year.
Personally, Straub was a delightful, unconventional man who marketed his eccentricities with the same skill he promoted his products. He was an outstanding amateur magician, appearing when time permitted on stages with professional entertainers. He also wrote voluminous letters especially in his later years pecked out laboriously on a typewriter, with a total disinterest in punctuation and exhibiting a freeform spelling that became identified over the years as Straubese. These letters have since become collectors items, as a few samples will illustrate.
For example, he wrote a trade magazine editor:
“You said in your letter the other day that you took the Liberty to call me F. J. But you forgot to say ACE HI O. H. F. J. Anyway, here is what F. J. wishes you to-do for the POOR Bricklayer.
Since you are going to have Plates made for the purpose of writing up some of the stuff that I was concerned with many years ago. And since it could be that I may live to be 50 or so, it could be that I would like to have the plates after you are through with them. As it could well be that some folks might want to read some of the trials and TRIBULATIONS (Say I did get thet big word in) that F. J. had to go through in getting people to think about read about and some few of them did buy some of the so called rediculis Cinder Blox.
14
For instance in Warren Ohio where straub patent cinder blox were Mfg. One time when I happened to be there a man came to our plant and F. J. showed him a service station that F. J. furnished the Blox for and layed up the job in red mortar. The man was so pleased that he said Mr. Straub if you will lay the Blox I will put up my new home out of your Blox. He was a pretty well known man in Warren so I said Man I don’t see how I will get the time to do but I will do it. The answer is a lot of folks saw his house and his wife was realy a big help for she sure was pleased to tell how they liked theirhouse.”

To another correspondent, he explained carefully: “This Type Writer is Garenteed to make no missspelling. But it could be some of the Gears are out of kelter.”
And, describing one of his early competitors, he wrote: A mr Eberling of Cleveland Ohio a Bricklayer made a machine that ashe said every time the machine breathed out comes a truly formed Blox paterned after the Clay tile real low cost tile. His Blox were used in some real Sky Scrappers in Detroit. His product was lets say 5 times as strong as the clay tile. But too bad were about 3 times as heavy. And since in partisions no great strength was needed so my good friend Eberling fell by the wayside. "Falling by the wayside" was a fate that eluded Francis J. Straub through a long and productive life. We will meet him again later in this story. But in the beginnings of the concrete masonry industry, he was a gust of fresh, shrewd. skillful and imaginative air that breathed some life and excitement into an industry that needed all of these things badly.
15
TheGoldenDecade
At the end of World War 1, the block industry was still pretty much a backyard operation. Usually the owner of a block plant worked as a laborer 12 to 14 hours a day. He had no time for selling block because he was too busy making them. The lack of vision, imagination and sales ability on the part of most manufacturers was a major problem.
Industry pioneer J. L. Pitha recalls that "investment requirements were but a very small fraction of what they are today. With $5,000 in cash it was possible to go into the block business in 1918. Major equipment consisted of two block machines and a mixer. A 750-squarefoot building was large enough to provide space to stack the block for curing.
Block were made in most unusual places then. One small manufacturer in the East worked with his wife in the cellar of their home every night after he came home from work. They mixed cement and sand on the floor by hand and then molded the material in a small hand machine. He made about 50 block every night that way. The next night, when they were cured, he would lift the block out through the cellar window and his wife would stack them.
It was recognized, even in those days, that heat was needed for curing, and in most of these small plants the only heat they would have in cold weather was a big pot stove. It was normal for the block nearest the pot stove to be "cured" better than those which were too far away, even though the "curing" was mostly drying out. However, the cement content was greater than it is today, and because it was necessary for the block to be hard enough by the following morning to permit stacking, calcium chloride was frequently used.
But in the post-war economy, conditions for this tiny, scattered, uncertain concrete block industry to become a large, powerful and important element in the construction field were almost exactly right. An exhaustive market survey made by the Portland Cement Association in 1919 indicated that the U.S. was some two million houses short of requirements, especially in the central states where concrete block manufacturers were then concentrated. There was also a powerful need all over the country for stores, schools. theatres and other public and semipublic buildings, long delayed by the war. And, between 1917 and 1920, coal had skyrocketed in price from 9¢ to $2.40 per ton, driving up the price of block's principal competition clay brick since coal made up about 10 per cent of the production cost of brick.
16 III
How well prepared was the block industry to take advantage of this potential bonanza? According to the same PCA survey, about 50 million concrete masonry units were produced in 1919 by some 2,000 manufacturers, of whom about one-third were adjudged large enough and stable enough to rate first-class standing. The same study revealed about 3,000 favorable locations in the U.S. where there were no block plants.
Before block producers could spread into these areas and take advantage of the market potential, however, there were some serious problems that had to be solved. The industry was in a deplorable condition from the standpoint of personnel, manufacturing equipment, quality of product and merchandising methods. Power equipment was almost unknown. Not more than a dozen fairly well organized plants existed. No attempt was made at the grading of aggregates, proper mixing or adequate curing. Quality products were practically unknown because no standards of quality were available. Building codes in a few localities gave some recognition to concrete masonry but quality requirements varied widely, and little, if any, attempt was made at enforcement. The result was that concrete masonry units were in ill repute generally and condemned by building departments, architects and reputable builders. The product was too unattractive to compete with clay brick, terra cotta and lumber on anything like price equality. Insurance rates were outrageously high; quality fluctuated wildly; building methods had never been standardized or even defined; promotion was non-existent; and the industry was unorganized and generally chaotic in such crucial areas as manufacturing, selling, cost accounting and advertising.
Typical of the confusion of this period was the situation in Wisconsin, where 8 x 8 x 16" block were selling in Janesville for 32 cents, while a few miles away in Madison where manufacturing costs were higher because materials had to be shipped in the same block was selling for 16 cents. Much of this economic chaos grew out of an almost total lack of cost accounting in the industry. Producers often didn't know they were losing money until they found themselves out of business.
Faced with these problems and opportunities, the block industry was floundering rather badly when the Portland Cement Association then less than five years old, itself called a conference of block producers and block machinery manufacturers in Chicago in mid-1919. The conference chairman. A. J. R. Curtis, head of PCA's newly formed Farm and Cement Products Bureau, told the assembled producers:
"The present high cost of lumber and the relative saving of time and labor by using concrete block construction constitute two arguments which would be working powerfully in our favor right now if we were organized to take full advantage of them.”
“After having studied several of the past attempts aimed at the development of the block business, we are of the opinion nevertheless that a carefully planned cooperative effort by machinery
17
manufacturers, interlocked with a similar effort on the part of the block makers, may be expected to succeed in creating and maintaining enormous new markets for block. It goes without saying that to develop the block business to the utmost requires the broadest vision. The man who pictures block possibilities in terms of foundations or porch piers need hardly expect to get his block used in great commercial structures.”
“The concrete building block is a product that can be successfully advertised cooperatively. The exact kind of block and process of manufacture has but a secondary interest to the public if the impression is made and maintained that all block are good. Prospective owners can be interested in the superior advantages of high class concrete building units, promoted jointly by concerns of unquestioned business standing throughout the country.”
The PCA immediately put its staff to work organizing concrete products manufacturers in several dozen major cities to mount a concerted attack to improve the quality of concrete block. The motives of the PCA, of course, were scarcely philanthropic. Only one million barrels of portland cement about one per cent of total cement production were consumed by block manufacturers in 1919; the PCA saw a potential for ten times that amount.
PCA's concern was shared and its goals applauded by a group called the Concrete Products Association, which had been formally established on March 6, 1918 and held its first executive council in December of that year in the offices of the Hydrostone Company in Chicago. Much of the organizational impetus came from a former member of the PCA Cement Products Bureau named W. R. Harris (who later became editor of Concrete Products Magazine). Under the direction of Harris, the CPA held its first annual convention at the Congress Hotel in Chicago. On Feb. 9, 1920, the Committee on Constitution and By-Laws of the new organization worked through the night to complete a set of objectives to put before their fellow members the following day. Thus on Feb. 10, 1920, the Concrete Products Association dedicated itself to:
Facilitate the acquirement and interchange of practical knowledge among its members;
Encourage the development of the art of manufacturing concrete products;
Create a standard of excellence in manufacturing;
Promote the use of concrete products: encourage and provide for advertising the products of members;
Gather data and issue bulletins of promotional character;
18
Exercise a corrective influence on the quality of the product to the end that Association standards may be maintained; and
Secure mo re efficient cooperation with the government and agencies thereof, as related to the concrete products industry.
The convention then elected J. K. Harridge as the first official CPA president and adjourned to spend the final day in joint session with the National Conference on Concrete House Construction. While the convention didn't add much to concrete technology, it did have the salutary effect of giving the various elements of the concrete products industry a better idea of how they must organize their forces to get anything done.
Three PCA men served as Assistant Secretaries from 1918 until 1942. These were Roy Peck (editor of Modern Concrete magazine in 1970), Dr. R. “Spec” Collins and E. W. Dienhart. During this period, PCA offices served as headquarters.
One of the early block industry leaders, Ben Wilk, recalls that “the number of manufacturers who were willing to pay even a small annual amount for trade association participation was not large. Most of the early annual conventions were of a technical nature and were scheduled for an extra day at the time of the annual convention of the American Concrete Institute. The active members were involved with both groups.”
The PCA, however, took a dim view of the national concrete products group, feeling that local and regional cooperative efforts were more likely to prove fruitful. At the same time, machinery manufacturers through the Concrete Block Machinery Association formed in July, 1919 were encouraged to cooperate more closely with products producers while curtailing the sale of machinery to people who lacked the financing and technical expertise to make it successfully in the block industry.
Through all these organization activities, PCA agents were buzzing like a swarm of inspirational bees. By the end of 1920, thirty-four local and two state concrete block organizations were in operation in addition to the two new national associations. These groups were subjected to constant pep talks and ego-building reassurance of the social importance of their product. Jealousies within the associations and the narrow vision of many of the erst-while backyard producers often made cooperative effort difficult, but generally this nationwide forced-feeding of an industry was tremendously effective to a large extent because block already had so many things going for it.
19
One of the most important was a very real cost advantage. A good grade of washed sand, delivered to the plant, would cost the block producer about one dollar per cubic yard. (The coarser material, called grit, was delivered at the same price.) Plenty of labor was available at 30 cents per hour. Portland cement discounted and credited for the return of the cloth bags in which it was then delivered cost about $1.50 per barrel. Despite these low costs of material and labor, block was selling for about three times as much as it brought 15 years later, and the demand was accelerating steadily.
Although this was due in part early in the decade of the 1920s to the shortage of other materials, there was the additional important factor that concrete block could be laid in a wall more quickly and at a much lower labor cost than could an equivalent volume of brick wall. For example, a common size of cinderblock that cost 20¢ in 1923 was equivalent in both size and cost to 11 clay brick. But the cost of laying up concrete block was more than 10¢ less than the cost of laying up the equivalent in brick.
The growing demand for block was also inspiring new and broader explorations by research and development specialists. For example, the first important broad-scale study of aggregates, mixtures, methods of curing and other factors entering into the manufacture of concrete brick was carried on during 1923 at Philadelphia in cooperation with Drexel Institute and the products manufacturers of that vicinity. Seventy different kinds of brick were made, varying in cement content, grading, and type of aggregates and consistency. The results of these tests conclusively proved the applicability of laboratory principles to manufacturing problems and pointed the way for improvements in quality and reduction of costs in products manufacture.
About the same time, several other important technological developments appeared on the concrete masonry scene. The use of washed sand became prevalent in the early 1920's, soon after Duff Abrams at Lewis Institute's Structural Materials Laboratory had come up with the water-cement ratio that converted the design of concrete mixes from a fortuitous accident to an exact science. Although the water cement ratio was supposed to apply only to the usual wet mixed concrete, it was found that it applied equally well to the semiwet mix used in making block. But dubious block producers had to prove this to their own satisfaction and did. Ben Wilk recalls working "on some tests where we took the amount of water needed to give the right consistency for block and we called that 100 per cent. Then we used 5 % and 10% more water, then 5% and 10% less water. We found that the excess water put us on the wet side of the Abrams curve and the smaller amount of water put us on the dry side, while the right consistency followed the Abrams curve for ratios of cement to aggregate almost exactly."
The work year for the block industry was also expanding with the technology. Before 1920, most of the concrete block plants in the northern part of the United States closed from three to four months during the winter. Thus when Spring came, the small stocks which had been accumulated disappeared quickly, and the producer had to play catchup all summer. Cold weather involved several difficult problems for concrete block manufacturers. Since it was
20
impossible to work the banks or pits for sand, gravel, and stone, sufficient aggregate had to be stored to run the plant for the entire winter and for a plant producing 3,000 block a day, this meant some 4,500 cubic yds. of storage space. In the few plants that attempted winter production, small reserves of raw material were kept from freezing by a steam coil installed underneath the pile, but major reserves had to be stored in large outside piles and the aggregate thawed as needed by several perforated pipes, five or six feet long, attached to the steam line. These pipes were driven into a portion of the pile, the area covered up with tarpaulins, and the steam turned on.
The principal drawback to winter operations, however, continued to involve the storing of large quantities of block, which meant tying up considerable working capital in finished goods inventory. But slowly the advantage of winter operations began to overcome the drawbacks. A growing number of contractors who poured foundations during the summer began using concrete block when it was available for winter construction. Materials such as cement were often cheaper in the winter, and it was also possible to provide continuous employment which made for more contented workers, lower personnel turnover and greater plant efficiency. When construction opened with a rush in the Spring, those block plants that had worked over the winter had a large supply of well cured block on hand and could give their customers good service. As a result of all these advantages, the stable, well financed members of the block industry began to operate year-round in the early 1920's.
During the same period, an immigrant bricklayer named Sigurd Bo was using his Scandinavian thrift to add to the technology of cinder concrete. Bo watched private scows dumping cinders into New York harbor under the cover of night while the city was paying out large sums of money to keep the harbor dredged. Bo suspected that most of the cinders could still be used as fuel. When he analyzed them, he found from 5 to 50 per cent of the fuel potential remained. He also knew that cinder aggregate was better with all the impurities burned out. So Bo developed a process for recovering the fuel and eliminating the impurities from cinder aggregate. It was patented in 1923 and assigned to the Cinder Products Corp. in Lockport. N.Y. five years later.
Meanwhile a revolution was taking place in the development of a wide range of other lightweight aggregates (described in detail in Chapter X).
The National Bureau of Standards had been assigned the task of research and experimentation on lightweight aggregate for use in Navy vessels in World War I. The first NBS working plant was a down-draft bee-hive kiln near Birmingham, Alabama, where enough aggregate was produced to supply the 3,000-ton "USS Atlantus," launched the following December at Brunswick, Georgia. The successful performance of this first vessel resulted in arrangements for letting two contracts for quantity production for other concrete ships then underway.
The fact that a lightweight concrete containing a cellular aggregate could be successfully employed in the building of oceangoing ships with 5" thick hulls and remain completely impermeable to moisture intrigued
21
designers and builders, and later established confidence among engineers and architects alike in the long-time performance of lightweight concrete. In 1923, Dan F. Servey, a graduate engineer and later president of the Haydite Company of Kansas City, produced the first block of expanded shale concrete masonry. The major block plants of the nation turned quickly in this direction, for it gave them a lightweight block with a high degree of insulation, and a uniform compressive strength equal to a heavy weight block.
Exhaustive physical tests confirmed the fact that expanded shale aggregate would adequately meet all concrete block specifications, and from that day on, the development of lightweight aggregate enhanced the esteem of the concrete masonry industry in the construction world. Haydite, the lightweight burned shale or clay aggregate, patented in 1918, was used increasingly by block producers during this period until by 1927, more than a hundred block plants were turning out Haydite block-30 to 35 per cent lighter than ordinary sand and gravel units.
But the real excitement of the golden decade of concrete block was not generated by technical developments. It came from one of the most effective promotional campaigns ever designed for a building product. The element besides consistency of quality most lacking in the early days of concrete masonry was imaginative promotion. Francis J. Straub took a giant step in the right direction, but he was one man and an industry approach was badly needed. That approach was finally provided in the early 1920's under the leadership of a group of aggressive and imaginative young men in the Cement Products Bureau of the Portland Cement Association.
Their most remarkable single accomplishment actually penetrated the White House in Washington and enlisted the implied endorsement of the President of the United States for concrete block. It was the sort of corny, zany adventure that couldn't happen in the sophisticated society of 1970. But in 1923 in the days of Prohibition and simple verities and a total lack of social complexities it could happen. And did.
In 1920 and '21, the PCA conducted a series of 31 home builders' short courses. Attendance varied from ten to 200 and included mostly block manufacturers, contractors and architects. Although the courses were designed primarily to furnish block producers with the information and inspiration to go out and sell their product, it was soon discovered that architects and contractors were equally interested in the possibilities of residential construction with concrete block. Because architects weren't familiar with detailing concrete masonry, the PCA published 25,000 copies of a house plan book that had to be reprinted twice in three years to keep up with the demand.
Encouraged by this show of interest, the promoters raised their sights and actually zeroed in successfully on the most visible target in America: the White House. The rationale for the promotion was the 100th anniversary of the writing of the song Home Sweet Home, a bit of Americana dear to the hearts of farmers,
22
merchants and presidents alike. Why not, reasoned the concrete promoters, rebuild the home that inspired the song by an odd coincidence built of white stuccoed concrete masonry and make it the center-piece for the observance of a "Better Homes Week?" And where, they asked, would it attract the most attention? On the White House lawn, of course. And so they took this outrageous proposal to Washington as part of a nationwide program of 36 widely scattered demonstration homes and ended up with the active participation of three U.S. presidents.
Secretary of Commerce Herbert Hoover broke ground for the house co-sponsored by the General Federation of Women's Clubs and the Better Homes in America League in mid-1922. It was officially dedicated by Pres. Warren G. Harding on June 4, 1923. During the months it stood on the White House grounds, it was inspected by hundreds of thousands of visitors, including the new President Calvin Coolidge, who toured it just before it was given to the Girl Scouts of America as a headquarters building, opposite the Corcoran Art Gallery in Washington.
In addition to the people who saw it in person, the house was pictured and written about in hundreds of newspapers and magazines, and a motion picture ostensibly from the General Federation of Women's Clubs but bearing the fine promotional imprint of the concrete people was shown in thousands of motion picture theaters throughout the country. The film had an added impact because it was the last public appearance of Pres. Harding before he departed Washington on the lengthy trip during which he contracted pneumonia and died.
Such promotions played a major role in the golden decade of concrete masonry during the 1920s, a period when all America was spending, and a large part of the money was going into building. The cement and concrete block industries were determined to move massively into this market, and they managed during the 1920's to knock down one-by-one the principal obstacles unfavorable fire insurance rates, punitive building codes, total lack of product standardization that stood in their way.
Probably the most stubborn roadblock in the early promotion of concrete masonry was the refusal of fire insurance companies to grant this product a competitive and realistic rate. The problem became a primary order of business at the first convention of the Concrete Products Association, where it was determined to set up an immediate program of fire tests with the Underwriters Laboratories to prove to a dubious insurance industry the firesafety of concrete block. The units to be tested were manufactured under the direction of the PCA's Cement Products Bureau in Sept., 1922. (The Straub cinderblock had been firetested six months earlier.)
The fire endurance tests-conducted on six 10 x 11' panels of 8 x 8 x 16" block and twelve smaller panels-began in December, 1922 and lasted for eighteen months. A final report was published by the Underwriters' Laboratories on May l, 1924. The performance under fire of the sand and gravel block was almost identical with that of the Straub block, and both received a classification of 2½ hours as a fire retardant.
23
But this was only a first step. High fire ratings were of no value unless the construction world knew about them, so block producers all over the country began sponsoring a series of demonstration fires in small test houses built of concrete masonry. The first demonstration was held in Lancaster, Pa. where the test building was 13 feet high and composed of two equal compartments. Oil soaked wood was piled in each compartment and a load of ten tons of pig iron was placed on the roof. A maximum temperature of 2,200 degrees F. was reached in one half hour, and at the end of an hour, the fire department turned a hose on the walls with no visible damage. The test was so effective in improving the local market for concrete block that the show went on the road, first to Chicago (for the fiftieth anniversary of the Chicago fire) then to Providence. R.I., Pittsburgh, Pa., New Kensington, Pa., Columbus, Ohio and points West. These demonstrations were planned to interest city officials, architects, engineers, builders, and prospective home owners in concrete block. And if they weren't interested, they were certainly aware something was going on. On the day of each test. the local fire department would go tearing through the streets of the city, attracting an audience to the burning. The show played to SRO crowds in Phoenix, Springfield, Cicero, Topeka, Birmingham, Indianapolis, and Los Angeles. In Minneapolis, the burn-out was staged on a main thoroughfare in the downtown area, and in Joplin, the fire was permitted to rage for 3 ½ hours.
What did all this heated activity accomplish? When the first block home was set afire in 1921, practically all states rated concrete masonry on a par with or below frame construction in fire resistance. By 1924, the National Fire Council was giving concrete block walls a two-hour fire retardant rating, and this classification was improved to 2 ½ hours in 1926 and three hours a year later. These ratings were printed and given wide distribution by the Concrete Products Association. Result: local and state insurance rating bodies began revising their schedules to reflect more favorable rates for concrete block, and by 1927, block was receiving the same rate as clay brick in 34 states.
Building codes were also getting concentrated attention during the same period. Until the mid-1920's, there were many building code provisions all across the country that unjustly restricted the use of concrete block. The 33 per cent maximum air space, for example, was outrageously unfair if a block with a greater percentage of air space could meet the gross area crushing strength test. Similarly, regulations calling for filling of hollow concrete block with concrete when the block were used in foundations increased the cost of the building unnecessarily. Also, many codes limited the height of concrete buildings and a few cities notably Chicago prohibited the use of hollow concrete block in foundation walls at all. The effect of this ruling was disastrous. For example, while Detroit was consuming 15 barrels of cement per year per capita in 1923, Chicago was consuming less than one-half barrel, largely because of the restrictive Chicago building code.
Thus much of the early effort of the various organizations promoting concrete block was aimed at getting these building codes revised. It was a tough, no-holds-barred battle, fought on every front and its principal battle lines were usually around the big city building departments. In some instances, public officials more-or-less
24
openly solicited "contributions" to permit block construction, and in some instances contributions were made. On a slightly higher plane, the specifications then being drawn up by the American Concrete Institute to control the quality of block also helped build credence with cities developing codes guided by the ACI specifications.
Jack Freedman of the Plasticrete Corporation in Medford, Mass. recalls that "in the Boston area only solid 12" concrete block was permitted below grade, making it very hard to work because of the weight. In 1922, with the help of Professor Walter E. Voss, of Wentworth Institute, I went before the State Legislature to have this ruling changed to 12" hollow and from then on, blocks in the Boston area market were used almost exclusively for housing foundations until poured concrete came in to destroy our market."
Similar efforts were taking place all across the country, and they were remarkably successful. By 1928, more than eighty city building codes had been revised to eliminate practically all of the legal obstacles to the increased use of concrete block. And in changing the building codes, the PCA and CPA missionaries were making sizeable progress before the brick and tile competition awakened to the threat. Quickly they began deprecating concrete block on every front possible. They also urged the bricklayers and masons unions to oppose building code changes and the inroads of concrete block on construction sites.
Convincing the bricklayers they should handle concrete block even in the face of a serious shortage of brick in the midst of a booming construction market was a tough job, and sometimes it took tough measures to get it done. A. V. Johnson of Omaha's Ideal Cement Stone Co. recalls that when our firm started making concrete blocks, the bricklayers refused to handle them because they were fearful that the fewer hours of labor required to lay a block wall would seriously affect their annual income. The founders of our business, Earl Peterson's father and uncle and two others, were former stone masons so they not only made the blocks, but marched out of their plant, rounded up crews of masons, and laid up the block themselves. The bricklayers remained adamant for almost three years, then went to Nels Peterson and said: "Will you get out if we agree to lay the block?"
He got out and that crisis was resolved, just as it was being resolved in dozens of other cities across the country. But even the successful modification of building codes in favor of concrete masonry sometimes created almost as many problems as it solved. In 1928, for example, a large concrete block manufacturer told a group of his associates:
"A building code, no matter how carefully worded, is worthless unless some provision is made for proper enforcement. In other words, it must have teeth. A properly enforced code is of priceless value to the reputable products manufacturer, for it not only guards him against shoddy and unscrupulous competitors, but is also an instrument of confidence building in his community.”
25
"Everything hinges on proper enforcement, and it is here that the products manufacturer can play a large part in making his code of value to himself. In the first place. he should make his own product of a high enough quality to comply with the code and enough higher to allow himself a safe margin if he has to deliver green products in order to complete some specific job falling under the code. Second, he should assist his brother manufacturers in attaining this standard of quality through personal contact or his trade association. And if his competitor refuses to make a product that complies with code requirements, then steps should be taken to encourage rigid building inspection and see it put off the market as harmful to all concrete products."
Once the campaign to revise insurance rates and building codes was well underway, the concrete industry representatives turned their attention to standardizing the product coming out of concrete block plants. In the early 1920s, the concrete block industry was in a chaotic state with respect to the sizes of concrete block. In that year, block were manufactured in 30 different lengths, 20 different widths, and 26 different heights. Architects were severely handicapped because they had no way of knowing what sizes would be delivered to the job until the block actually arrived. They were, therefore, unable to dimension their buildings with any assurance that the units actually delivered would correspond to the dimensions.
During 1923, this confusion stimulated the industry to request the Division of Simplified Practices of the National Bureau of Standards to cooperate in establishing standard sizes for concrete block. The American Concrete Institute, the Portland Cement Association, the Concrete Masonry Association, and the machinery manufacturers were all represented in preliminary conferences, and on Oct. 16, 1924, a general conference was held in Chicago. A schedule of sizes of concrete block, proposed by Committee K-1 of the American Concrete Institute, was considered and standard sizes were adopted, restricting concrete block to one length, one height, and four widths, and by 1927, ninety-five per cent of all concrete block were produced in conformity with these standards.
Block had by then increased its share of the masonry market from 13 per cent (in 1922) to 20 per cent, and speakers at the CPA convention in 1927 emphasized the newly developing use of concrete block as a backup material. For the first time, overcapitalization was stressed by one speaker who pointed out: "I'm not making a plea to return to the backyard method of plant operation, but I do believe that the manufacturer who meets these new challenges successfully will have a plant capable of running two or even three shifts a day rather than a plant operating at capacity only part ofthe time."
An advertising agency executive named Austin F. Bement admonished that same convention:
“As an association, you can afford to undertake in cooperation, the important work of general public education. Five per cent of your last year's gross volume of sales would amount to $7 million. Many industries particularly while young, can and do afford to set aside 10 per cent, and
26
in some instances, even a larger proportion of their gross sales, for the purpose of protecting their present volume of business and to build new and enlarged markets.”
“Let us be extremely conservative in considering your problem from the standpoint of the industry as a whole and consider what you could accomplish through the appropriation of two per cent of your gross sales. With $2.8 million to expend annually in educating the American public to accept and demand concrete products, you could do a considerable job nationally, to supplement local and regional efforts.”
“You gentlemen are interested in a fundamental thing building a market for concrete products and you have banded yourselves together behind a program which seems admirably well rounded on paper. If it fails it is not the fault of the program it is your fault. Your potential market lies in the 2.4 million homes of the United States. In the final analysis, there is no reason for you to expect the architect, builder or contractor to do your selling for you.”
The conventions in 1928 and 1929 that ended concrete block's golden decade began to take on the overtones of conservatism that tend to infiltrate revolutions once they have achieved their original goals. In 1928, most of the talks at the CPA convention dealt with relatively sophisticated programs of sales promotion to meet the competition now acutely aware of the inroads of this new industry. Rock Products reported that “Conversation in the lobbies adjacent to the convention hall indicated that the industry had ‘grown up’ and was assuming a seriousness not recognizable at previous conventions.” The same atmosphere prevailed in 1929, when one of the CPA's prime movers, Wallace I. Harris, suggested that the Association's work was too big to be left to volunteer workers and the CPA now needed some paid employees to give full time to the job of popularizing concrete block with the public. This was in February, 1929, when the economy was still burgeoning and the prosperity balloon gave promise that it might grow indefinitely without bursting.
Block producers were still looking ahead then. Had they been inclined to take a backward look in 1929, they would have seen the most spectacular decade of growth and progress in the concrete block industry, before or since. Production of concrete block during this period increased 774 per cent, from 50 million units in 1919 to a peak of 387 million equivalent 8 x 8 x 16" units in 1928. Production increased every year with the exception of 1920, when a cement shortage forced some plants to close.
During this same period, the number of concrete block plants declined about 40 per cent. In 1920, there were about 7,000 plants in the United States; this had decreased to 4,140 plants by 1928. Immediately after World War 1, the number of block plants increased dramatically, and very quickly capacity began to outstrip demand not only by the influx of new producers, but even more by the increased productivity of improved
27
block machines, and this resulted in intensified competition that drove many of the smaller block producers out of business. The 4,140 plants in 1928 were producing 700 per cent more block than 7,000 plants in 1920. Between 1921 and 1928, the number of concrete block manufacturers making more than one million units annually increased from one to 28.
Jesse Besser, thinking back on the golden decade of concrete block, singles out two developments as the most important of that era: The substitution of plain, smoothfaced block for the rock facing of virtually all block up to that time, and the development of modular dimensions when a good many new block makers needing such boundaries were coming into the business. At the beginning of this decade, a plant producing a thousand block a day was large, and there was a conscious effort to make the units look like rock; after all, stone was used to build basements, and wasn't that what block was for? By the end of the decade, this point of view seemed as obsolete as the pyramids of Egypt or the possibility that anything could happen to derail the headlong express plummeting the American economy to progressively more spectacular way stations of prosperity.
The greatest coup of the block promoters in the early days or in any period, for that matter was the building of the replica of the concrete house that inspired the writing of Home Sweet Home on the grounds of the White House where it was seen by hundreds of thousands of visitors. Then Sec. of Commerce Herbert Hoover turns over the first shovelful of dirt for the foundation of the house. Workers swarm over the halffinished structure. After completion it is dedicated by President Warren G. Harding, standing at the front door, surrounded by assembled dignitaries.

28
TYPICAL COST OF MANUFACTURING, 1928
1,200 block per 10 hr. day Size standard 8” x 8” x 16”
250 operating days per year
Materials & Labor
Cost for 1,200 block Cost for block
Cement 70 sacks at $0.65 $45.50 .037 Aggregate 18 cu. Yds. at $2.00 36.00
Direct Labor
1 operator at $6.00 6.00
1 off Bearer at 4.00 4.00
2 helpers at 3.50 7.00
1 Mixer Man at 4.00 4.00
Daily Labor 21.00 .018
Manufacturing Liability Insurance 1.50 Expense Water .60 (Per Day) Fuel (Curing & Heat) 1.50
Power & light 1.50
Repairs to equipment 1.00 Breakage 1.75 Miscellaneous 1.00 .007
TOTAL DIRECT COST 110.40 .092
General Expense
Depreciation-Equip. 25% of $4,750.00 $1,187.50 Depreciation-Bldgs. 5% of 5,400.00 270.00
Interest on Invest. 7% of 20,150.00 1,410.50 Taxes & Insurance 300.00 Land rental 6% of 5,000.00 300.00
General Expense Per Year 3,468.00 13.87 .012 General Expense Total Daily Cost 124.27 General Expense Total Yard Cost Per Block $.104
To this cost must be added selling expense, delivery cost and profit to determine selling cost.
TYPICAL ESTIMATE
CONCRETEBLOCKMANUFACTURE,1928 Production–1,200–8’x8’x16”blockdaily.
MACHINERYSCHEDULE
BUILDINGINVESTIMENT
MainBuilding $2,500.00 Palletsat30¢ each 450.00 Curing equipment, CarsandTracksor includingboiler LiftTrucksandRacks 1,100.00 andpricing 900.00 Mixer 400.00 CuringTunnels 1,200.00 Motor 200.00 MaterialBins 600.00 Shafting,Belts,Etc. 100.00 Contingent 200.00
Machine $1,500.00
ScreenandMaterial conveyor 500.00
Installation7wiring 250.00 Tools 100.00 Miscellaneous 150.00
TOTALMACHINERY $4,750.00
TOTALBUILDING 5,400.00
TOTALPLANTINVESTMENT $10,150.00
ADDITIONALOPERATINGCAPITAL 10,000.00
TOTALCAPITALINVESTMENT $20,150.00
29
IV Gallery of Early Concrete Masonry Buildings

Concrete block was sadly and generally regarded as a fine material underground or as back-up for some other facing in the first few decades of its life in North America. But even during those years, there were visionaries in the fields of architecture and building who saw concrete block as much more than that and who had the courage to convert their convictions to tangible form.
Pictured on the following pages are a cross-section of the works of a few of these pioneers along with some of the more conventional uses of concrete block prior to World War II.
30

31
Depression
W. D. M. Allan, new manager of PCA's Housing and Cement Products Bureau, told the Concrete Products Association's 1929 convention in New Orleans: "Every thoughtful business man in our industry knows that we are in the last days of the pioneering stage and just about ready to step out and take a regular place in the established masonry field. Like many others, our industry has gone ahead more or less blindly, increasing output without regard to sales and has been able, because of an increasing general market, to get by. But the market has changed and in order for us to make progress we must take inventory and select a new course. No industry or individual can make progress if every little obstacle deflects it from the chosen course, but it is no little obstacle that we face, and it is just as important to be able to adapt ourselves and select a new course when the one we are following proves to be wrong, as it is to persistently follow the right course once it is chosen."
A look around the convention floor made it clear that one new course desperately needed was a broadening trade association base that would attract the meat and potatoes and not just the dilettantes of the concrete block industry. The doom of the old Concrete Products Association was probably sealed at the New Orleans convention, when only a handful of delegates appeared and only a third of those were concrete products manufacturers. The tiny attendance gave all present both a chance and a cause to speak, and the speakers were brutally frank. Most agreed that the CPA had failed to win prestige or attract membership because it had never undertaken large scale activities of nationwide interest to the industry.
A new name for the Association was suggested, not just for the sake of changing but because of the firm belief among those present that the far-reaching activities proposed should not be associated with the organization that had so little accomplishment to its credit. The annual dues were increased to $100 for the largest plants (producing 500,000 or more units annually) and $50 and $35 for smaller plants. Thus did the Concrete Masonry Association step forward to take the place long occupied by the National Concrete Products Association. Whether it would represent a change in philosophy as well as name remained to be proven. (The organization didn't formally adopt the name National Concrete Masonry Association until the annual meeting in Toronto in 1934).
In the aftermath of its declaration of a new name and new principles, the leaders of the Concrete Masonry Association predicted it would attract all of the financially sound and well-managed plants in the industry.
32 V
Commenting on this prediction, Concrete Magazine said:
“It will be well if it comes true, for undoubtedly the salvation of the industry lies in its ability to cut loose from the irresponsible price-cutting element that is in business one year and out the next, only to be replaced by others of the same breed. Partly through mergers and partly through the more painful process of business mortality, the incompetents must be eliminated if the industry is to flourish.”
“Even if only a few hundred of the larger companies, were to give financial support to the Association, the larger dues now established will create a fund sufficient to carry on the most important of the proposed activities. Such a group will be financially able to do things in a big way. Through diversification of products, better sales methods, cooperative advertising and other modern methods of business, the competition of other strongly organized masonry materials can be met, and new fields for concrete masonry units can be developed. All this does not mean that the little fellow is to be frozen out. The little fellow who is competent will in due time grow up to the size of the community in which he operates.”
The presidency of the new organization was put in the potent hands of D. R. (Spec.) Collins, who had served the old organization as secretary for a number of years, during which he had been a voice in the wilderness crying for sound, aggressive industry wide merchandising policies. Now he had the authority and the support to run with his views, and he wasted no time setting them forth in a communiqué to the industry that said, in part:
“This is not a cigarette advertisement but a straight shoulder-to-shoulder talk about concrete masonry. First off, let's get together and speak plainly about the things that affect our industry. I have in mind our mutual interests the present and future interests of those engaged in the manufacture of concrete masonry units.”
“By getting together, by becoming affiliated with and backing the Concrete Masonry Association we can do ourselves more good than we possibly could through efforts expended in any other direction. The time has come for us to get together and bring ourselves out of the haphazard class. And you will have to admit, much as we hate to, that things have been haphazardly done in the industry these past few years.”
“The proposed program developed for the CMA is rather lengthy, necessarily so because a laxity in the formulation of such a program during the past five years has caused an accumulation of needs that must be squarely faced. It is a program that says in no uncertain terms that the
33
weapons that must be used in winning a market for concrete masonry are RESEARCH and EDUCATION. Within the next month every concrete products manufacturer will have an opportunity to study over this program and aid in carrying it out. If the industry is really looking forward to its own development, there will be spontaneous support, for this program presents an opportunity to see how seriously the concrete products industry takes its own business and its future.”
The new five-year program was keyed to the assertion that "intelligent merchandising is the thing most needed in our industry." The aim was simply to increase the market for concrete masonry to the point where every progressive manufacturer might benefit, and the first steps to include a sales manual, monthly newsletter, a formal research program, a planned program of national advertising and publicity and, of course, stronger efforts to build the membership.
For the first time in its short history, the concrete block industry began to hire salesmen on a large scale in an effort to sell more block. In 1929, some 400 salesmen were employed in the industry, and the number was increased to 940 in 1930. They had a tough job to do, because the architects, contractors and bricklayers then controlling construction had served their apprenticeships when "cement block" first began to be generally used for foundations. These men had formed their impressions at that time, and they weren't easily changed. But many of the new salesmen were both ingenious and aggressive. Fairly typical of this breed was the block salesman who was making a strong plea for the sound insulation value of his products, based on some laboratory tests. When the architect wasn't impressed, the salesman suggested that the architect and his specification writer accompany him to a nearby hotel, where part of the partition walls were built of concrete masonry and part of clay tile. They went into one room and asked the telephone operator to ring the phone in the next. It sounded like an alarm clock where the clay tile partitions were used and could hardly be heard where concrete masonry was used. The next day, the architect brought his client to the hotel and tried the same stunt on him. It worked and it sold the job for concrete block.
Looking back over the first year of the revived concrete block industry and its new-look Association, Spec Collins pointed proudly to an imposing list of accomplishments that included: an increase of 14 per cent in the number of industry salesmen; aggressive promotion of cooperative selling, especially in Minneapolis and Milwaukee; increased use of block in large buildings; greater diversification of products; and substantial improvements in quality, especially in lightweight units.
34
But all of this, unhappily was the last gasp of the wonderful nonsense of the 1920s, a sort of industrial whistling past the graveyard. Although no one could yet see it or would admit it if they could all the new salesmen in the world couldn't prevent, or even mitigate, the catastrophe upcoming for the concrete block industry, the nation and the whole world.
There had been some strong hints but no one was listening. For example, in 1929 construction activity started a precipitous decline from its 1928 peak (by 1933 it was only about 25 per cent of the 1928 level). Since the demand for concrete block derived entirely from the construction industry, block sales declined by a similar percentage. At the same time, excess capacity that had been gradually building up became acute in 1929 with the decline in demand. The industry capacity that year was estimated at five times the number of block actually made and sold, and the problem was intensified by the fact that a similar situation prevailed in the common brick and clay tile industries.
The combined factors of a skidding economy, overproduction and large capital investment resulted at first in a round of wild cut-throat competition. Most producers had little knowledge of their actual costs, and as a result, many block companies reduced their prices so far they couldn't cover their out-of-pocket expenses. Thus, when the crash came, there was an immediate high mortality rate among producers. In 1929, fifteen per cent of the block plants went out of business. The bankruptcy rate was high, many plants consolidated or merged, and some producers left the business because they were convinced that concrete block was finished as a building material. There were a good many indications that they might be right. In 1930, common brick was getting 47 per cent of the total masonry business; clay tile, 23 per cent, and concrete masonry, 30 per cent. Common brick sales fell off more than twice the decrease suffered by concrete block, so as far as share of available business was concerned, concrete block made substantial gains in 1929. But overcapacity in all building materials was completely out of hand. Brick, clay tile, and concrete masonry plants combined could produce a total equivalent of 60 billion brick a year and the demand was for 15 billion and going down precipitately. Thus overcapacity was the cancer eating into the vitals of the entire building materials industry.
Overcapacity was further exacerbated in 1930 by the increased use of multiple shifts and piece rate incentive systems. As the profit margin on each block declined, many producers stepped up production in an effort to build total profits to old levels through sheer volume. There were three types of incentive plans in use in concrete block plants. In one, the foreman was paid for all labor, usually at the rate of two cents per block. This led to profiteering by the foreman, complete disregard for maintenance of equipment, and no increase in production.
A second method was the definite apportionment of pay among all of the men. In most cases, two cents was given to the group for each block produced. Thus the more units the group turned out, the more each worker received. The third plan called for the payment of the mixer operators, machine operators and the
35
off bearers on a piece rate basis. The laborers handling the movement of block from machines to curing room, curing room to the stock piles, and later onto the trucks, were paid a straight hourly wage. In all of these systems an attempt was made to classify the work so that the pay of each worker was in relation to the skill required to perform his job.
The building decline in the United States started in May, 1928, and amounted to an average loss of $2 billion (or more than 30 per cent) a year. Residential was the hardest hit, and since 80 per cent of block production went into the residential field, the industry was mortally hurt. Block producers carried all their eggs in one basket always a dangerous thing for any industry. Several large manufacturers saw this danger in time and made it a point to develop new markets for block and such allied products as floor filler, fireproofing tile and roof slabs which could be easily manufactured without much additional equipment or plant rearrangement. But generally, 1930 was a disaster, with the decrease in block sales running between 15 and 20 per cent.
Another early casualty of the stock market crash and the depression was one of the most provocative and potentially useful organizational developments to come along in the block industry in many years. A group of far-sighted block producers in Milwaukee decided around a luncheon table in January, 1929, that they could best meet the problems all of them shared by an effective cooperative approach. Consequently a few months later, the Milwaukee Concrete Products Cooperative Association opened its doors, rolled up its sleeves and went to work.
The goal of the Association was 100 per cent membership in Milwaukee County, but it achieved only three-fourths of that over the 15 month life of the organization. With this nucleus, however, the group did some exciting things.
First, an Association testing machine was acquired and members taught to use it. Strengths doubled and producers were shown that good materials and careful mixing cost no more than shoddy work. Very quickly, builders in the area learned that block carrying the quality imprint of the MCPA meant just that.
Next, the Association established a successful credit control system. Billings and collections were done through a central organization. All accounts were carefully investigated, and delinquency was reduced virtually to zero and this in a period of specially tight money. The Association also did a considerable amount of collective advertising and sales promotion work. Members found that contractors were willing to pay an extra 2 to 4 cents to keep the block market in a stable condition and be assured of a quality product. Contact was made with every Association job at least once a day, block was delivered at the right time, in the right place and the right amount and massive good will was built with the people who design and construct buildings.
36
Then the Milwaukee banks jacked interest rates out of sight, residential construction dropped off drasticallyand the Association became a victim of serving a market that no longer existed. In the immediate aftermath of the dissolution of the MCPA, prices tailed off 40 per cent and the cutthroaters took over the field, a commentary as depressing as the economic conditions of the time. An obituary in Concrete Magazine called the MCPA "the most advanced attempt the concrete products industry has ever known to apply proven business methods in a co-operative effort to solve its problems." And that it did.
By 1933, concrete block production had skidded to 45 million units from the 1928 peak of 387 million. Many plants had gone out of business, and many others were idle. The block makers who were operating were fighting among themselves for the small amount of business available by price cutting, ridiculous credit terms and other dangerous concessions. The flavor of the day was caught by a price list put out by R. E. Hamilton's Sons, Detroit, in 1934. "Competition," shouted the black headlines, "has gone crazy and we are forced to the belief that Barnum was right. But, when in Rome, do as the Romans do . . . so, here are our New Low Prices on Concrete Products."
And so it went. Competition did go crazy, and prices kept going down, down. Ben Wilk remembers that "the depression struck Detroit very hard. From 26,000 housing starts annually during the 1920's, building permits dropped to a low of 323 housing units in 1932."
Jack Freedman of the Plasticrete Corp. in Medford, Mass. recalls: "In 1930 we took the Straub franchise for our area. Then the depression set in and things really went bad, not only for us but for the entire country. As if that weren’t bad enough, in 1933 the brick layers union in Boston tried to pass legislation to prohibit the use of block and we really had to fight to defeat that bill. Then in 1934, the union changed its bylaws to demand that masons require two men for every block over 40 lbs in weight. This bill would be presented every two years before the Massachusetts Legislature and we would keep shooting it down until it finally faded out of the picture. My brothers and I had to work in the plant because business was so bad in 1933. We only did $18,000 for the entire year and then the Roosevelt Administration began to pump construction money into the country and business started to pick up."
The United States Government took several steps in 1933 to relieve these depressing conditions. Under the National Industrial Recovery Act passed in June, 1933, the Concrete Masonry Association was designated as the trade association for the concrete products industry, and a code of "fair competition" to eliminate price-cutting was worked out. The general reaction of the industry to the Act and the code was favorable. Hours of labor, rates of pay, and fair trade practices were set up; prices became common knowledge and therefore were no longer an important competitive factor in sales. The emphasis switched from price to quality and service. The avowed purpose of the NRA was to eliminate chiselers from the
37
industry. It was not an attempt to fix prices but rather to cut out the foolish practice of selling below cost, of not knowing what cost is, and of cutthroat competition.
NCMA president Ben Wilk was named Code Authority for the block industry, and Horace Bush was appointed Secretary. Wilk recalls that "it was our function, primarily, to see that prices remained stable. I traveled constantly to various cities to talk to local block associations about the necessity of controlling prices."
Even though the Federal Specifications Board had approved specifications for concrete block for the use of all government departments, it was still seldom selected for government buildings. In 1933, the NCMA sent Spec Collins to Washington to convince government officials that concrete block should be used in all types of government buildings. Both the NCMA and the PCA worked long hours with government departments, and by the following year, practically all of them were specifying concrete block. It was used for backup and partitions in much of the Post Office construction, and the Bureau of Indian Affairs of the Department of the Interior specified concrete block for the construction of hospitals, schools, and quarters. In Army construction work, concrete block was specified for exterior wall, partitions and backup, and the Department of Agriculture used it for warehouses and experimental laboratories.
In 1933, several government agencies were set up to purchase concrete block. The Public Works Administration was probably the most important. Public works construction by state and local governments had declined steadily until, in 1933, it had virtually ceased. Allotments were made that year for such projects as schools, hospitals, and public buildings, using large quantities of block. Other newly formed government agencies, such as the Home Owners' Loan Corporation and the Agricultural Adjustment Act both created in 1933 were of help to the concrete block industry. The Home Owners' Loan Corporation made money available for home modernization and repairs, and the Agricultural Adjustment Act improved the economic position of the farmers and placed cash in their hands. This helped revive the farm construction market, which had almost vanished during the early years of the depression.
In July 1935, The National Industrial Recovery Act was invalidated by the U.S. Supreme Court, but it had, by then, performed a valuable service for the concrete block industry.
Although business activity was in a constantly deepening trough of despair lifted only by public building programs the decade of the 1930's was surprisingly productive in a good many technological areas for the concrete block industry.
38
Ben Wilk recalls "During the Depression we had plenty of time on our hands. and we looked for things to do. This led me into an extensive series of tests on the use of high early strength cement in concrete products plants. I got the idea from a PCA publication called Temperature Effects on Strength of Concrete.
“Preliminary tests using one high early strength and one ordinary portland cement gave such interesting results that two additional series of tests covering all of the high early strength cements ordinarily available in our market were carried out in our plant in 1934 in cooperation with the Concrete Products Assn. of Detroit, and the results were reported at the ACI convention in 1935.”
“A committee was then organized to study the use of high early strength cements in concrete products manufacture. Two years later, the Committee reported: “It would seem that on an average 70 pounds of high early strength cement will give better results than 94 pounds of normal portland cement during the first 28 days in the manufacture of concrete masonry units.”
In connection with the ACI tests on high early strength cements, a study was also initiated on the effects of the grading of aggregates. Course sand had long been preferred to fine sand, and the phrase "coarse particle predominating" was frequently used in specifications. But products’ manufacturers found that too much coarse aggregate while giving greater strength would honeycomb the block face.
Prof. Duff Abrams, in his pioneering work on concrete, had introduced the Fineness Modulus idea of comparing one aggregate with another by making a sieve analysis. Using this method. Prof. Abrams could prove what had long been assumed: that coarse aggregates gave better strength. With this as a jumping off place, Ben Wilk and Detroit chemical engineer William Grant made a number of tests on ten combinations of 3 x 6 cylinders prepared with various aggregate gradings. The results of these tests indicated that in making concrete block with sand aggregate, the most desirable Fineness Modulus is 3.74.
Throughout the depression years, the NCMA also sponsored a comprehensive program of tests conducted at the Underwriters' Laboratories and the research facilities of the National Bureau of Standards, the University of Wisconsin, and the University of Illinois, where a number of load tests on concrete block were run in 1931. Using the results of these latter tests, the NCMA prepared a booklet entitled Facts About Concrete Masonry, which it circulated widely to promote the use of concrete block. It has since become a construction industry best-seller many times over.
The Portland Cement Association equipped with all the necessary devices to make sample block and conduct standard fire tests was busy researching, too. The PCA laboratories fire-tested 215 concrete masonry walls over a five-year period during the depression. Some of the important findings of these tests included:
39
The fire endurance period of concrete masonry walls is independent of the type of mortar used. It does depend slightly on the character of the mortar joints, but mostly on the type and grading of the aggregate and cement content of the block;
Application of plaster finish to either the exposed face or both faces of a block wall substantially increases the fire endurance period and wall strength of the units;
The compressive strength of concrete masonry walls is in direct proportion to the original compressive strength of the units;
Unit design has no bearing on wall strength after fire exposure for walls of the same thickness;
Concrete block walls offer substantial load-carrying ability and safety before, during, and after severe fire exposure.
The various relationships established by the tests provided important basic information, both for the manufacture of concrete masonry units from the wide range of available materials and for their assembly into walls which would meet the exacting requirements of regulatory bodies as to fire resistance and strength.
The PCA conducted other useful research during this period, including tests on the moisture penetration of concrete block walls indicating that the proper application of two coats of portland cement paint would prevent the entrance of wind-driven rain. These tests and the pleasing appearance of painted concrete block walls encouraged builders to make greater use of painted block in exposed construction.
There were also some drastic changes taking place in machinery for the manufacture of concrete block (described in detail in Chapter XIV). The two most far-reaching developments were the concept of compaction by vibration and the plain steel pallet, which made possible the production of various sizes of block on the same machine. The vibration patents of Louis Geldman were purchased by Eugene Olsen and the Stearns Manufacturing Company which came out in the mid-30's with the revolutionary Joltcrete machine. About the same time, the Besser Company was incorporating its plain steel pallet in a three-at-atime machine known as the Vibrapac and a new era in block production was on hand, with early models capable of producing six hundred 8 x 8 x 16" blocks per hour.
A machine developed i n the early 1920's to make concrete ashlar also came into broad use during the depression years. Because the manufacture of ashlar block required extra time and labor, very little was done with it during the booming business of the '20s. Manufacturers didn't want to waste time on ashlar
40
when they could sell all the standard block they could make. But in the depression year of 1931, concrete ashlar was reintroduced to try and shore up a desperately sagging market for block. The timing proved to be right this time, and ashlar was widely used in the 1930's in such structures as churches. schools and many public buildings where architectural beauty was of prime importance. This opened a new market and a new concept for concrete block.
At the same time, some spectacular advances were being made in the discovery and development of lightweight aggregates (treated in detail in Chapter X). Between 1930 and 1938, three new lightweight aggregates called "Pottsco," "Waylite," and "Superrock" were patented. All were manufactured from slag aggregates prepared by special processes. The expansion of lightweight aggregate capacity during this period including such established products as Haydite and Celecrete, as well as the newcomers was an important contribution to the concrete block industry. It was equally important that these aggregate plants were being located within economical shipping radius of more and more concrete block plants. The advantages of lightweight block were so great that the future of the concrete masonry industry became closely tied to the developments in lightweight aggregate. Builders, architects, masons and bricklayers all preferred the lightweight block. Cinders were still used more widely than any other lightweight aggregate but, in many instances, the supply of the right kind of cinders was inadequate, and the market for cinderblock began losing ground to other types of lightweight aggregates.
This, however, didn't deter our old friend, F. J. Straub, who simply refused to be put down by either a Depression or growing competition from the new aggregates. In 1934, F. J. secured a patent on a process for troweling concrete masonry units as they were being manufactured. His trowel featured moving side plates which oscillated rapidly across the front and back of the block while the mold box was being filled and the block tamped and stripped. The oscillating face plates could be installed on any type of stripper machine.
Even more than technical innovations, however, the concrete block industry in the depression years needed the Straub wit, and he came through in fine style in advertising his new invention. In January, 1936, a full page ad in CONCRETE Magazine under the large, black headline, "Straublox", said in part:
After I had invented OSCILLATED STRAUBLOX and was ready to give a license agreement, the first thing that was settled in my mind was: I would have willing royalty payers.
Now, how was this to be done? Well, to make a man Happy, let him be Free. That is: Do not tie him up to pay so much per year regardless of how many blocks he sells, but only ask him to pay on what blocks he sells each month; and let him cancel any time he wants to.
41
My license agreement is written with these two ideas in mind. It is not a long, tiresome paper full of legal entailments. It is short and to the point and is easily understood.
Some folks have asked me: Why allow a licensee to cancel whenever he wants to? My reply is that a man who knows the game will never cancel; and anyhow, if he wants to stop oscillating, he surely should be free to do so.
One fellow said: Why make a WATERPROOF block when the rain can go through the mortar joints? My reply is that there is ten times as much surface in the blocks as in the joints. There are more joints in a brick wall, but this does not prevent architects and people from using brick.
And one time a fellow who looked like a banker said: “Can more money be made by Oscillating?” Certainly, because we will now replace more of other materials and we will get a lot of people to use CONCRETE BUILDING UNITS who refused to use them in the past.”
Although the NRA was dead, the adrenalin it pumped into the block industry continued to promote health and growth. While a good many other basic industries continued to struggle in the late 1930s, the block industry began to show some unmistakable signs of revival.
Jack Freedman remembers that "in early 1936, the block business was picking up. We could produce about 5,000 blocks per day, although the Boston area couldn't yet absorb them."
By late 1936, many concrete block plants were once again working at capacity. In some areas, plants could have sold more block if they could have increased their production. The bottleneck was usually curing chamber capacity, and the timely research on the use of high early strength cement made it possible to reach a given degree of curing in a considerably shorter period of time than ordinary portland cement permitted. Because this expanded the capacity of the curing chambers and permitted increased production, the use of high early strength cement became general in the late 1930's in spite of its extra cost.
The first convention of the NCMA not tied to the American Concrete Institute was held in Detroit in 1936. At that time, a bustling assistant manager of the PCA's Cement Products Bureau named Elmer Dienhart was supervising the activities of the NCMA on a part time basis. No one knew, then, that this was merely a preliminary to a much more direct relationship.
The 1936 convention seemed to say, rather loudly, that the NCMA members had emerged from the depression strengthened and revitalized. It was the most successful convention in industry history, bringing together a surprisingly large contingent of producers from all over the nation in a stirring
42
demonstration of the industry's recognition of the value of the Association. According to Concrete Magazine, "the 1936 convention touched off an industry-wide wave of enthusiasm and marked the beginning of a dynamic drive for recognition in the masonry construction field."
The growing importance of the related machinery industry led to the inauguration, the following year, of the Concrete Industries Exposition in conjunction with the NCMA convention and it has been a fixture ever since.
Things continued to look up in 1938, when the Public Works Administration reactivated its program and pumped $1.6 billion of construction projects into the economy. The Works Progress Administration also became a large concrete block customer, spending more than $14 million on concrete products in the late depression years.
The United States Housing Authority began supplying financial assistance to local housing in 1937 in the form of capital loans to aid in financing construction projects, primarily to help keep rents down. This slum clearance construction was extensive and used large quantities of concrete block. In 1939, twenty per cent of all residence units built were constructed under the U.S. Housing Authority program, and more than half were made with concrete as a principal wall material. Construction activity and concrete block manufacture continued to expand in 1940 and '41; the latter year set a record for block production of 467 million units (the first time the industry's output equalled in wall area the combined output of clay brick and hollow clay tile). A large part of it, however, was needed for a new and burgeoning element in our economy called national defense. A war had been raging for two years in Europe, and uneasiness in the United States was growing daily. Along with it grew the defense establishment and the demand for concrete block.
When war came to the U.S. in December, 1941, concrete block was an essential, major industry still suffering with a minor-league self-image, anchored to the days of backyard production and industrial anarchy. While the United States girded to fight a global war, the concrete block industry fought and won a parlor revolution, from which it emerged with a trade association and an industry image more in keeping with its size and responsibilities.
43
This is how a typical concrete masonry price list looked during the depths of the Depression in 1933.
CONCRETE PRODUCTS
Price List Effective August3,1933
PLAIN BLOCKS
ROCKFACE OR PANEL BLOCKS
Sx8xl6 Plain Blocks 10 8x8x16 Face Blocks 13
Sx8x8 Plain Halves 09 8x8xl6 Corners Face Corners 22
Sx8x8 Plain ½ Corners l0 8x8x8 Face Halves 12
Sx8x16 Plain Corners 14 8x8x8 Face ½ Corners 17
8x8xl6 Plain Pilasters 16 8x8xl6 Face Slotted 20
Sx8x16 Plain Slotted 16 8x8x8 Face Slotted ½‘s 16
Sx8x8 Plain Slotted½'s 12 4x8x16 Face Slabs 13
8x12 x16 Plain Blocks 14 16x16 Chimney Blocks 32
8x12 x12 Plain Pier Blocks 16 16x20 Chimney Blocks 42 8x12 x8 Plain Halves 12 Each Opening Extra 05
8x12x16 Plain Corners 17 8x12x16 Plain Pilasters 20 Terms, Net - Plus 3% Sales Tax
Sxl2x8 Plain ½ Corners 14 Prices Subject to Change Without Notice 8x12x16 Plain Slotted 18
Sxl2x8 Plain Slotted ½ ‘s 15 4x8x16 Plain Slabs 10 4x8xi2 Plain Slabs 10 8'and 10" Joist Slabs 10
44
Agroupofblockindustrypioneers gathers at the Multiplex Concrete Machinery Co. at Elmore, Ohio in 1933 to watch a demonstration of the original Straub oscillating attachmentforblockmachines
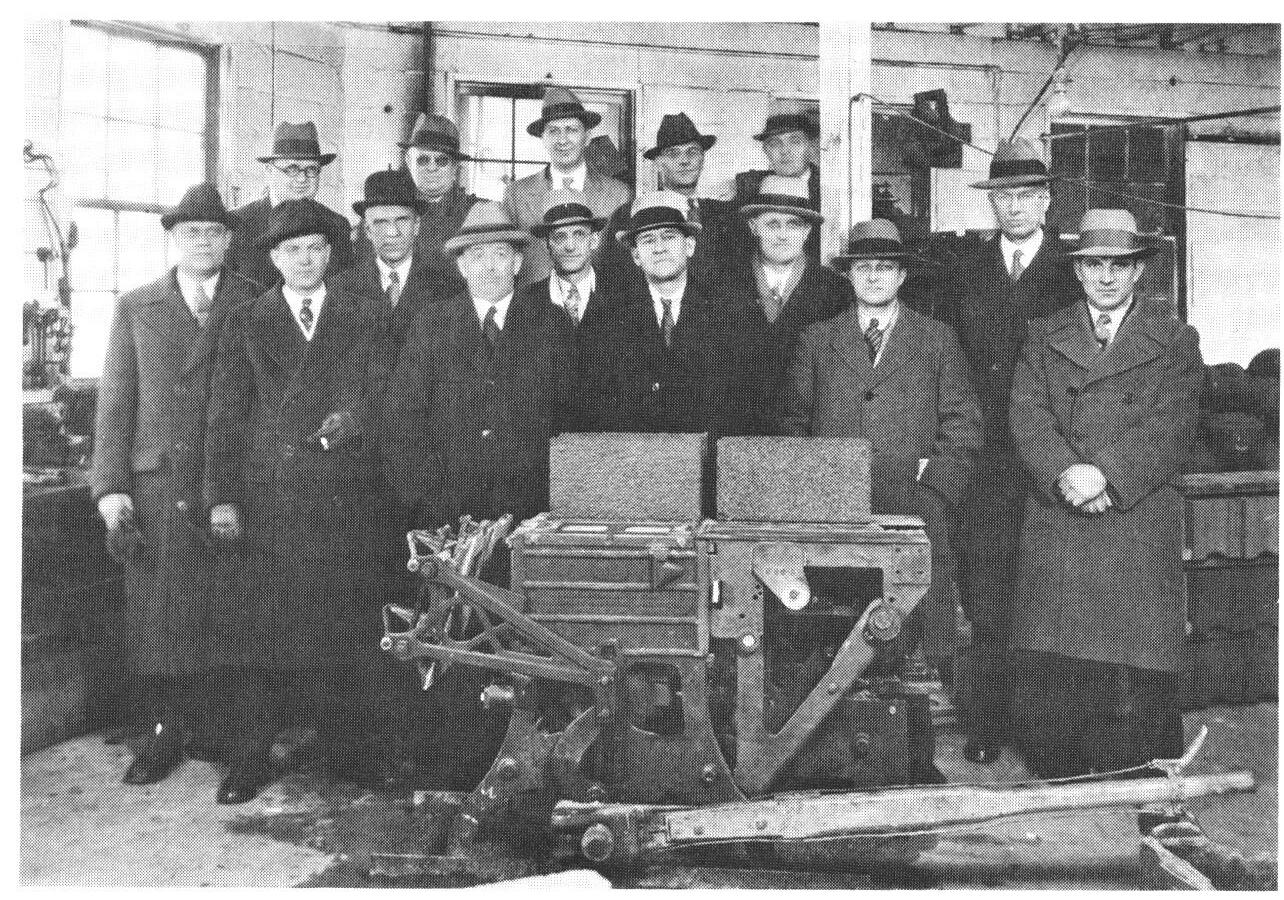
Even the latter stages of the Depression didn't hold down a large turnout at the NCMA convention early in 1938. Here, a group of block makers attending that convention enjoys a banquet sponsored by the Besser Company at the Sherman HotelinChicago.
45
The Rebirth of The National Concrete MasonryAssociation
When the United States was plunged into World War 11, the NCMA had functioned for a decade as an affiliate of the Portland Cement Association by paying a membership fee of ten dollars per year. This small fee made it possible for the Concrete Products Division of the PCA to send out some letters and a small bulletin from the Chicago headquarters, but it didn't begin to cover the total expenses of the Concrete Products Division which, at that time, was headed by William Kaiser as Manager, with Elmer Dienhart as Assistant Manager and Mrs. Evelvn Bouette as Secretary.
These three people did a fine promotional job for the NCMA. It is impossible to evaluate the tremendous groundwork that Kaiser and Dienhart performed for the concrete products industry which, at that time, was more or less in its infancy.
By 1940, when new and more automatic block making equipment, developed by the machinery manufacturers, resulted in higher block production and intensified competition with clay products and lumber, it became apparent that the NCMA needed a self-sustaining, independent organization. This conclusion was underscored by the construction needs imposed on our government by World War 11.
And so 1942 became a year of decision for the NCMA. The war, with its tremendous demand for materials of all description, made it necessary for the President of the United States to appoint a board with the responsibility of controlling manpower and production in the manufacturing fields. From the War Production Board, subcommittees were appointed to control the respective trades. The building material division was headed by an administration well known to concrete products manufacturers. This was a great help, considering the weakness of the NCMA at that time.
Because the brick, tile and lumber industries each had a strong association and powerful representation and connections in Washington, they had a considerable advantage over the concrete products industry, especially in obtaining support for government construction work. Accordingly, at their annual meeting in 1940, the Executive Committee and the Board of Directors were instructed to proceed with plans for the re-organization and strengthening of the NCMA by establishing a self-sustaining, independent organization with its own office
46 VI
and staff. This would ultimately bring about a greater prestige and respect for concrete block with the Building Materials Division of the WPB.
In 1942, at the annual meeting in Buffalo, J. L. Strandberg was elected president of the NCMA and charged with the responsibility of reorganizing the Association to be fully independent of any outside affiliation. It was also decided to conduct two other regional meetings to inspire the manufacturers in various parts of the country to support the declaration of independence made in Buffalo.
After these meetings (in Kansas City and Atlanta), the Executive Committee (consisting of Walter Manhardt, Ray A. Berger, and Harold Spaight) was empowered to proceed with the reorganization. This required additional meetings and much correspondence, culminating in a meeting of industry leaders in Detroit on November 6 and 7. Present at that historic session were:
Ray Berger
Jesse Besser
Louis Brookman, Jr. J. J. Buzzell H. A. Davis E. W. Dienhart
Cloyd Fellabaum
Walter Manhardt
Earl Petersen
R.Marshall
Roy McCandless
E. F. Olsen Haakon
Paulson Fred Reinhold Harold Spaight
John L. Strandberg
Benjamin Wilk
A comprehensive statement of the issues and problems confronting the industry evolved from this two-day meeting and set the stage for NCMA's independence. Major points in the statement included:
(1) The growth of the industry and the shift from many small plants to fewer large plants pointed up the need for a full-time staff.
(2) The War Production Board had indicated that block production was inadequate. In order to insure allocations of materials for replacements, repairs and maintenance, the industry would necessarily have to work in close relationship with the Concrete Products Section of WPB.
(3) One of the most important problems of the industry for the next year was expected in the area of manpower. Many plants had more orders than they could fill, yet were only able to run at 50-75% of 1941 production. It was felt that eventually national manpower legislation would be passed, at which time a strong organization should he available to represent the industry.
47
(4) Since regulations of OPA having to do with maximum prices bore a very important relation to all concrete masonry unit plants, adequate centralized representation needed to be established to safeguard the best interests of the industry.
(5) Since having to do with hours and wages were becoming increasingly important, the industry needed to be prepared to cope with them.
(6) For the next year, it would probably be necessary to pool facilities in order to serve large projects; in many cases it might even be necessary to move existing equipment to the site of projects in remote areas.
(7) Centralized aid was already needed for handling priorities for repairs and new equipment. Such aid would be of even greater importance if, as expected, the industry was confronted with allocation of raw materials and labor, as well.
(8) Specifications adopted by government agencies for controlling quality were becoming of greater importance. Therefore, the industry needed to be alert to insure the adoption of reasonable and fair specifications for all types of concrete masonry units.
(9) After completion of the war-time construction program, the industry would need an organization to cope with situations arising from greatly reduced production, especially that of finding means of continuing in business.
(10) The industry must be alert to the necessity of coping with post-war problems and prepared to advance its interests in securing a large share of the expected extensive postwar construction program.
(11) Under the existing circumstances, it was the obligation of every manufacturer to support his trade association. First, because of the direct benefit to his business; second, because of the indirect benefit received from recognition of his industry; and third, because of the general benefit of assisting in the preservation of American industry.
(12) Initiative in any successful enterprise must spring from the progressive elements within that enterprise. The Executive Committee believed that most concrete masonry unit manufacturers are progressive and accordingly anticipated the full cooperation of the industry.
48
(13) A trade organization worthy of its name will conduct its affairs to reflect general benefit to members and non-members alike. Many of its activities could, however, be directed for the exclusive benefit of its members, and it was the purpose of the National Concrete Masonry Association to specialize in activities of specific benefit to members.
(14) The extensive promotional activities of the Portland Cement Association in support of concrete masonry units was recognized and appreciated. In due course, the National Concrete Masonry Association hoped to be in a position to augment these activities and so solicited the continued promotional support of the PCA.
It was at this Detroit meeting that the rebirth of the NCMA became a reality. The Constitution and By-laws were worked out, approved and adopted. The first year's budget of $40,000 was decided upon and steps taken to raise this money without delay. A list of manufacturers deemed capable of pledging $500 each was drawn up and approached. Gene Olson of the Stearns Manufacturing Company, and Jesse Besser of the Besser Corporation each of whom had volunteered support up to $10,000 as needed to reach the goal were appointed to head the soliciting committee. However, the mission was so well accomplished by telephone and telegraph that $15,000 of the amount was raised by the evening of the second day, and the budget was well in sight. It was a great victory for this pioneering group. In the aftermath of the meeting, Stearns and Besser loaned their respective advertising managers to the NCMA to make up a brochure which was distributed to all members and prospective members.
Here are some of the highlights of that brochure:
Ten years ago the concrete products industry made the equivalent of 200,000,000 8 x 8 x 16" units. The 1941 production exceeded 500,000,000. How many units can it sell in 1942? How many in the post-war years, when the dammed-up demand for construction breaks loose and competition among materials will be still fiercer?
In these days, business profits by organization by the interchange of ideas between men engaged in similar activities, by many men putting their shoulders to the same wheel.
The National Concrete Masonry Association has served those purposes well and continues to serve them. The work has developed upon a few willing enthusiasts that is always true in young organizations.
49
Today the industry and the NCMA face a challenge. Meeting it successfully calls for the participation the serious active participation of a wider circle of concrete products manufacturers.
The growing competition, not only of other masonry units but also of new non-fireproof materials, is costing your industry untold thousands of dollars in war work contracts. It will be felt even more when peace comes.
To defend its present position to enable it to offer the war effort its best service to build business for the future, for small plants and large ones, the concrete products industry must strengthen its Association and expand its activities.
This industry has come of age. It is no longer a backyard sand pile and hoe affair. It has sizable investments to protect it has a brilliant future to achieve. Your Association is beginning to function on a scale to command the greater respect of all elements in government and in construction fields. To bring to its members maximum benefits, the National Concrete Masonry Association is embarking upon a definite, realistic program.
This is not a peanut stand business. It's a big business. This program outlined requires money. For the first year it needs a minimum of $40,000. That's modest for an industry doing a $70,000,000 business!
To get the ball rolling, a group of manufacturers have advanced $500 each to underwrite the initial expenses of setting up the expanded organization. All the other plants that are so urgently needed to insure wide, democratic participation in the direction of the effort are now invited to come along on a basis that is considered fair and equitable to all concerned.
The immediate positive response was enough to launch the NCMA on the broad base that all block manufacturers wanted, and shortly after these inspiring early days, President Strandberg wrote the following letter to William Kinney, then general manager of the Portland Cement Association:
The situation confronting the concrete masonry unit industry at this time convinces our Directors of the necessity for expanding our organization in order to cope with many new problems.
Attached is a copy of the minutes of our Executive Committee meeting held recently in Detroit in which you will find outlined some of the major problems which we face. We realize that most of these problems can be dealt with only by direct representation of our industry. At a meeting of our Executive Committee in Chicago on November 28 it was decided to employ a full-time staff to carry out the program outlined in the Minutes of the Detroit meeting. As you know, we have arranged with
50
Mr. E. W. Dienhart to serve as Executive Secretary in the management of our activities. In this connection, our Executive Committee has requested me to convey to you our appreciation for your cooperation in releasing Mr. Dienhart so that he could accept the position with our organization.
It is our plan to eventually establish separate headquarters offices. Until such time as we do set up our own offices it would greatly convenience us if you would grant us permission to continue our headquarters at 33 West Grand Avenue with the understanding that you would be at liberty to terminate this arrangement at your discretion.
I have also been requested to convey to you the appreciation of our industry for the excellent cooperation you have extended in the promotion of the use of concrete masonry units and we sincerely hope that our action in enlarging our activities will in no way lessen the extent of your promotion activities in extending the market for concrete masonry construction.
Thus the umbilical cord that had nourished the NCMA through its early years was officially cut. In January, 1943, a permanent office of the NCMA was established in the First National Bank Building in Chicago, properly staffed and ready for the annual meeting in February, 1943, of the revitalized and reborn NCMA.
51
War—and Post War
Almost two decades after the beginning of World War II, a pioneer of the block industry would look back at the re-birth of the NCMA in 1941 and say: "The real program in our industry began with John L. Strandberg. This man was not only large physically, but also large in intelligence and courage. He saw that the industry could no longer depend on the PCA and other related organizations for its help, and he strongly urged that we hire our own full time staff and strike off on our own. I remember the board meeting at which that decision was made very well. There were many misgivings, but John Strandberg felt the time was ripe, and he advocated getting a group of manufacturers to underwrite a minimum budget. Through this time of doubt, John never wavered. His strength and foresight carried all of us through."
In 1941, the relative handful of people who believed in concrete block as an integrated, important industry that should attack its problems cooperatively needed both strength and foresight in ample amounts. Although the evidence to support their point of view was profound, the inclination in the industry to act on it was-as usual-almost nonexistent.
A spot check taken of the construction field in 1941 revealed that less than eight per cent of the potential customers for concrete block knew anything about it. And this ignorance was especially acute among government officials who were passing up concrete block by the millions in planning public buildings. "A $75 million industry," wrote John Strandberg, as president of the Concrete Building Units Company in Kansas City, Mo., "has been asleep at the switch while other products of a lesser value but with a collective effort have succeeded in getting much greater recognition. And we stand by and wonder why!"
At the time Strandberg made that remark, the NCMA membership rolls showed 262 paid-up members (and 26 in arrears). The NCMA had historically ridden the coattails of the PCA or the ACI; there was relatively little pride of accomplishment as an industry, little sense of need or urgency for cooperative action, and even less inclination to be assessed in any realistic way to pay for this cooperative work. This was the situation in 1941 when other, highly organized competitive industries began picking up a lion's share of the war construction work simply because not enough people knew the advantages of concrete block.
Strandberg told it like it was when he addressed the 1942 convention as the NCMA's new president. "We open our annual convention this year," he said, "in the midst of war." Conditions entirely different from any which have ever confronted our industry are before us. In searching for past experience to help guide
52 VII
us through these hazardous times we become aware of the fact that during the last war there was no such thing as an organized concrete masonry unit industry. We have gone a long way during these past few years. We now represent a major industry in the building materials field. As such, we have obligations not only to our own members and to all the industry, but above all we must adjust our affairs in support of the united war effort.
The group of industry leaders who met throughout the summer of 1942 with Strandberg were determined to do something about this. Their success while certainly a reflection of the urgency of the times was also a tribute to their tenacity and dedication. But it wasn't easy ever. After the original group of large companies had pledged to underwrite the revamped NCMA's first budget with $500.00 contributions each and independence was assured, a letter was sent out to the remainder of the members explaining what had been done, asking for opinions on expansion of the NCMA and approval of the new dues structure.
The directors had labored long and carefully over the problems of dues, attempting to work out a schedule to meet the best interests of everyone concerned. They hit on 1/50 th of one cent for each 8" x 8" x 16" unit manufactured, a figure they considered so inconsequential that there could be no real objection. A minimum annual limit of $25.00 was established, representing dues based on a production of 125,000 units. It was thought that producers with a lower production figure would probably derive more benefits in proportion than the larger producers and would therefore be willing to pay the proposed minimum. At the other end, a top limit of $200.00 was set for plants producing a million units annually. Here it was felt that the Association could not render proportionate service to firms making more than one million units.
Replies straggled in and many of the respondents objected to the supposedly foolproof dues structure. Sadly, Strandberg wrote one of them: "I am certainly sorry that you have voted as being opposed to undertaking the program of work which has been outlined. It does seem that sooner or later, the manufacturers of concrete masonry units must come to realize that they have a responsibility to the general welfare of the industry and that a start should be made in that direction to set up an organization which can independently represent the best interests of our own particular business."
Even some of the original $500.00 pledges failed to appear, and most of 1942 was spent by Strandberg and his associates literally organizing the industry. (In soliciting sponsors for the underwriting fund, participants in the Concrete Masonry Research Association were passed by on the correct assumption that a later arrangement could be made to merge the two organizations. Similar treatment was accorded members of the National Cinder Concrete Products Association, which had merged with another group of producers to form the Cinder Masonry Research Association. In April 1944, the latter merged with NCMA, uniting all segments of the industry for the first time.)
53
Slowly painfully slowly the membership took shape and form in the aftermath of a succession of persuasive letters sent out over Strandberg's signature. "It would give me much personal satisfaction," he wrote, "if your firm would accept my invitation to join us. Advance payment will cover the cost of dues for at least two years and will provide our treasury with sufficient resources so we may aggressively and confidently complete our organization and get to work on the tasks requiring immediate attention."
One of the most immediate tasks, once sufficient backing was assured, was the selection of an Executive Secretary to run the newly independent NCMA. However, the need for paid staff was questioned and this turned out to be almost as much of a hassle as raising the money. As late as August, 1942, an industry leader was writing Strandberg: "I realize, John, that you are anxious to put the industry on a solid footing, and I agree with you wholeheartedly. On the other hand, there are so many uncertainties that the average manufacturer would not respond and furnish the necessary foundation to carry on a worthwhile program. Those of us who have been close to the industry for many years are proud of its achievements and can see a big future ahead. Frankly, however, I don't think we can get enough support at the present time to take care of a program including an executive secretary. The ground work should be laid, however, by constantly driving at the representative manufacturers. In this way they will be right for the idea when the psychological time comes along."
He was wrong. The psychological time had come and, so eventually did the money. And on Nov. 28, 1942, the Executive Committee of the NCMA meeting in Chicago, passed the following resolution: "Because of the urgency of the situation, immediate steps must be taken to set the organization in motion. A number of candidates for the full-time management of the Association have been considered. Final decision, carried unanimously, is that the NCMA engage E. W. Dienhart for the position of Executive Secretary effective Jan. 1, 1943."
The decision wasn't reached easily, and the unanimity of the final vote didn't reflect the differences among industry leaders that preceded it. The differences were finally resolved, however, and on Dec. 1, 1942, John Strandberg wrote Elmer Dienhart:
"We are starting on a big venture which I have long wished for and always had in mind you would head as executive secretary. However, things started to look pretty dark for a few days last week, even to the point where I began to doubt that you actually were cooperating with me one hundred per cent. Now that things have been cleared up, I know that you meant business and always gave me the fullest cooperation. Nobody could sway me until you and I had gone through a third degree. I expect you realized the hard task I had in conducting this trial I felt was unjustified. I only did my duty and so did you, and I found out that you were one hundred per cent just what I expected. From now on you may rest assured that no one can change my opinion. You will definitely have my full
54
support, and it will be a great pleasure for both of us to have this association recognized in every corner of our country."
The new working director of the NCMA was well qualified for his assignment. Elmer Dienhart started his business career in 1915, as a general contractor specializing in concrete construction. Three years later he joined the Portland Cement Association staff as a field man, and in 1921 was assigned to the Cement Products Bureau. In the late 1920's he served as general manager of the Acme Concrete Products and Gravel Co., Cement City, Mich., and later as sales manager for the Maul Macotta Corp., of Chicago. In 1932 he returned to the PCA where he spent most of his time on the road, promoting concrete residence floor construction and precast concrete joists with considerable success.
Now the new NCMA team had been selected, and it was time to go to work. There was plenty of work to be done. Two months before Dienhart took over his new job, the NCMA Executive Committee had decided "that the many new problems arising from effects of the war warranted the holding of our regular annual meetings on Feb. 16 and 17 at the Hotel Sherman, Chicago. The meeting will be compressed into two days and the banquet and other entertainment eliminated. The over-all theme will be `How Concrete Masonry Manufacturers can Help in the War Effort,' and invited speakers will include important representatives of the various government agencies with whom our industry is directly concerned."
From that meeting came a blueprint of wartime activities for the block industry and an imposing list of immediate and urgent problems that had to be tackled. Among these problems were:
Making an industry survey to serve as the basis for allocation of materials and especially for replacement and repairs, with the various appropriate governmental agencies;
Finding ways and means to insure the delivery of products of uniform high quality;
Tuning the concrete masonry industry to the tempo of the all-out war effort by finding markets in war projects and developing uses for concrete masonry in new fields opened up by the war;
Adapting concrete products plants to special products required for the protection of life and property;
Preparing the industry for the expected enormous reconstruction period after the war;
Changing the still generally unfavorable attitude of bricklayers with regard to concrete masonry units; and
55
Continuing and expanding research activities for the solving of future and existing industry problems.
NCMA President Strandberg had already been busy trying to resolve many of these problems. Even during the travail of re-organizing the NCMA and hiring an executive secretary, Strandberg was firing off a barrage of letters in the interests of the block industry in general and NCMA members in particular. Strandberg didn't tilt windmills. Instead he took dead aim on the top men in government or industry who could help, then he went straight to the point. His letters through this critical period make up virtually a chronicle of the history of the concrete block industry in World War II.
One of Strandberg's favorite pen pals was Harry S. Truman, who was not only the Senator from Strandberg's home state of Missouri but was also chairman of the Senate's powerful Special Committee to Investigate the National Defense Program. On April 17, 1942, Strandberg wrote Truman: "Attached is a report showing the comparative costs of four different types of wall sections prepared specifically for the contractors, engineers and architects on the Sunflower Ordnance Plant at Eudora, Kansas. We prepared this report to show these gentlemen that the concrete products manufacturers in the Kansas City area can produce materials to build the walls of these buildings at the same or less, cost than wood.
All that the manufacturers of concrete products want is a chance to submit bids on these buildings on a fair and equitable basis. This is not a precedent, as the specification on the Wahoo Ordnance Plant in Wahoo, Nebraska, were open to three types of materials, wood, concrete products and clay products and this plant is identical with the one to be built at Eudora, Kansas. I might also point out that at the Gardner Air Base, the contractor has been slowed up tremendously because of the slow delivery of sized lumber. This will not be the case if concrete products are used, as the plants in the Kansas City area can deliver to the contractor any quantity of masonry products he may require."
A month later, Strandberg traveled to Arkansas to have a look at a new concrete block plant in Malvern under O. D. Leming of Vibracrete Concrete Products. He ran into instant trouble, typical of the times. Camp Robinson was being built nearby in Little Rock, and there was a tremendous need for building materials to construct a large housing project. Vibracrete's offer to supply 130,000 concrete block was turned down summarily by the contractor. When Strandberg and Leming protested, they were told that the architect, a Mr. Van Valkenburg, wanted nothing to do with concrete block. So Standberg shot off a testy letter to the head of the Federal Housing Authority, saying: "Mr. Van Valkenburg met us with the most ungentlemanly reception I have ever experienced from anyone. He came out in the reception room and after looking over our cards crushed Mr. Leming's in his hand and tossed it over towards the reception desk at which time I retrieved my card to prevent the same procedure. I have personally met many men in all walks of life, but never have I received such discourtesy. Without giving us any information or an opportunity to present our case, he walked right out on us with a beastly look on his face. I know it is not
56
the policy of the F.H.A. to have men of this caliber in their employ. I feel that Mr. Van Valkenburg has challenged the industry I represent and the Association I am heading and ask that you use your good office to get this matter clarified so we may know where we stand in regard to our product in the State of Arkansas."
A month later, Strandberg was at it again, this time chiding G. B. Arthur, Chief of the Concrete Materials Section of the War Production Board over a WPB press release that outraged Strandberg's sensibilities. "During the past two weeks," he wrote, "the press has featured many news stories extolling the advantages to be gained by substituting clay products in place of lumber. These articles were prompted by WPB release No. 1814. Naturally, we are chagrined to find our industry ignored, especially when we know that the use of our products has so much more to offer in the effort to find a practical means to relieve the acute lumber shortage.
"Now please don't get the reaction that we expect W.P.B. to take over the task of selling our products for us, because such is not the case. We do, however, believe it would be an aid to the war effort if our product was given the recognition it deserves and if the full capacities of our plants were utilized."
While the NCMA was slowly winning this recognition for the block industry the federal government imposed an ironclad ban on private construction. This didn't adversely affect many block makers because the demand for block for war plants and war housing facilities kept most manufacturers busy. In the later part of 1942, the War Production Board urged the nation's concrete products manufacturers to increase their output to help offset the estimated 1943 lumber shortage of 6 billion board feet. Block production also released transportation which was on the critical list for other uses. In most cases, the raw materials necessary for the manufacture of concrete block with the single exception of cement were locally available.
Also in 1942, the NCMA was asked by the War Production Board to make an intensive and accurate survey of the material requirements of the concrete masonry industry. The request was labeled urgent and the full cooperation of every manufacturer expected.
Block producers were told that "if our industry is to be accorded the consideration we say it deserves, it will be necessary to back our claims with proof. This is a case where we can't ‘Let George do it’ because at some later date when an individual plant needs help in getting materials, it's going to make an awfully big difference between having the survey report and not having it."
In spite of this growing recognition of concrete block and frantic activity on behalf of the industry however, block production declined in 1942 to 392 million units and continued to decrease in 1943 and 1944, skidding to 260 million in the latter year. Lower production was obviously not the result of lower demand, rather it was
57
caused by labor, and equipment shortages in the industry. All of the large block machinery manufacturers had converted their factories to making war goods. There were therefore, no new machines with which to expand production or replace worn out equipment. In addition, the supply of repair parts was reduced to a trickle, which meant much "machine-down" time and many makeshift repair jobs which lasted for only a short time. Delivery trucks were also in short supply and the labor problem was even worse because the military services had drained off much of the manpower. Many plants that had operated two and three shifts in 1940 were gradually forced to return to one shift because of insufficient labor, and in some plants, machines were completely idle. High rates of absenteeism also aggravated the labor problem.
The vital need for construction materials had prompted occupational deferments for some workers in this field. In answer to a request for clarification of the position of the block industry, Major Ernest M. Culligan of the national headquarters of the Selective Service System told a group of assembled block manufacturers bluntly:
"The 10 million fighting men must come from the youngest and healthiest and generally most effective of the 60 million manpower reserve. This means, beyond any question, that those men who are fit for military service, but who are temporarily deferred as "necessary men," must ultimately be replaced either by men overage or not fit for military service or by women. This is definitely the long-range responsibility of the employer. Occupational deferments are temporary usually for a six month period. They are granted when a man is impossible or difficult to replace the time the deferment is granted. This is a temporary consideration, and the Selective Service System will be sympathetic to nothing less than maximum effort by employers to train substitutes for all such men. The granting of a deferment is the Government's contribution to your business. The training of a substitute is your contribution to the nation's business of waging total war."
By late 1942, the shortage of construction materials had become so acute that Sen. Truman's committee was investigating. And part of the problem continued to lie in the fact that in many instances concrete block was being overlooked in areas where it could have been supplied to provide quick, low cost structures originally designed for lumber. And so Strandberg once again wrote his old pal, Harry Truman:
"A recent issue of the New York Journal o f Commerce announced that your committee is undertaking an investigation with the hope that more lumber might be supplied both for war and civilian use.
We wish to take this opportunity to lay before you information showing how concrete masonry construction can be used advantageously in conserving lumber and other scarce materials. The use of one standard concrete block, 8" x 8" x 16" in size, will save about three board feet of lumber. While the concrete masonry industry produced approximately 500,000,000 units in 1941, there was
58
an unused plant capacity of about 65% which in terms of lumber replacement equivalent, would be close to 3,000,000,000 board feet.
Manufacturers of concrete masonry units are widely distributed throughout the United States. There are approximately 3,800 plants, of which 800 are of large capacity. In general, concrete masonry plants are located near the center of markets where the bulk of building materials are consumed. Raw materials, used in making concrete masonry units are plentiful and geographically distributed so as to require a minimum of transportation."
Strandberg described eight major advantages of concrete block including: savings in critical materials; availability; surplus capacity; transportation economies; portability; surplus labor; low cost; and speed of erection. He then concluded:
“In our opinion, measures to be taken to relieve the lumber shortage through the use of masonry should include the following suggestions which we have made to the Concrete Materials Section of the War Production Board:
Have the Army, Navy, Maritime Commission, and other governmental agencies add details for masonry construction to all standard plans issued by them;
Instruct headquarters and field staffs to make every effort to substitute masonry for lumber regardless of the fact that standard plans show lumber;
Send similar instructions to architects, engineers and contractors engaged in design and construction of camps, ordnance plants and housing;
Call on the organizations representing the clay products and concrete masonry industry for detailed information on the availability of materials for each project;
Check with the bricklayers' union for information relative to the number of masons available for each project."
At the 1943 NCMA convention in Chicago, Pres. Strandberg, his job of organizing done, was moved upstairs as chairman of the board and Walter Manhardt became the new NCMA president. One full day of the convention was devoted to talks by representatives of federal government agencies. War transportation
59
problems prevented mounting the Concrete Industries Exposition in conjunction with the NCMA convention. In spite of this loss, however, an encouraging 400 members were on hand, and all the convention sessions were well attended.
The major technical problem distressing the producers present was the growing restiveness among builders over shrinkage. During this war period, when the demand for concrete block constantly outstripped production, stock piles quickly vanished, and green block were shipped to job sites. Many reputable producers did this with extreme reluctance and with a warning to the buyer that these block were not ready for use in building. The result was that many uncured concrete block structures developed excessive cracking, a fact which alienated many officials, builders, and architects who were formerly friendly toward block. This later became a serious handicap in building a permanent expansion of the market for concrete block, and industry technicians were directing many hours to seeking and disseminating various means of preventing shrinkage cracking and still meeting wartime construction demands.
There was also a great deal of disillusionment over the prices fixed by the Office of Price Administration for concrete products. (See Fig. 46) The prices varied state-by-state. and most producers felt they had been pegged unfairly and unnecessarily low. Jack Freedman in Boston, for example, recalls that "when the war broke out, we were going great guns. Then we were frozen at a low price by the OPA at 13 cents per 8inch block and we couldn't get labor as they were also frozen at a low labor scale. So the owners had to go back to work in the plant, because we were making a lot of block for the construction of barracks and industrial buildings for the war, and also thousands of blocks for ballast." This was a fairly typical reaction of block producers during this period.
There were other technical matters attended to, one of them a highly unusual step to be taken by an industry on its own initiative. At the suggestion of its members, the NCMA forwarded a request to the American Society for Testing Materials for an upward revision of the specification requirements governing the quality of hollow load-bearing concrete masonry units. In acknowledging this formal request, the Secretary of the A.S.T.M. committee said that within his knowledge this was the first time an industry had requested the adoption of more stringent requirements for the use of its product.
The growing trend toward lightweight aggregate also came in for a good deal of attention, stimulated to some extent by a unique shipbuilding project on the West Coast. During World War I, concrete ships of lightweight aggregate were built, but the end of the war had stopped both talk and production. Now, in the midst of World War II, the number of existing ships was fast dwindling because of the submarine menace and this, coupled with the tremendous demands upon the steel industry for war material of every kind, caused the U.S. Maritime Commission to cast about for a satisfactory substitute for the traditional plate steel in shipbuilding. Engineers poured through the records, still preserved in detail, of the shipbuilding program
60
of World War I, during which 14 vessels were successfully built of lightweight concrete. Now America required nearly ten times that number. A series of conferences were held to determine the most practicable and effective steel substitute, and as a result of these conferences, several American shipbuilders actually got into the production of concrete ships. Although the results never threatened to replace conventional ship design, it did serve to call the possibilities of lightweight concrete to the attention of a great many people.
It was, perhaps, a poor time to do this because in the late war years, the trend toward lightweight concrete block had been reversed by severe shortages of lightweight aggregates. The supply of cinders the major lightweight aggregate had been sharply reduced when the public utilities began using powdered coal, which gives no cinders. Although the manufacture of other lightweight aggregates was meanwhile expanding, the extent of this increase during the war years was limited by the sizeable capital necessary a minimum of $250,000.00 to start a Haydite plant, for example.
Such lightweight slag aggregates as Waylite and Celocrete had to be manufactured near a blast furnace on steel mill property, and the steel companies at that time were hesitant to sign contracts permitting aggregate plants to build there, apparently having little interest in this type of disposal of their slag by-product. The bulk of lightweight aggregate in proportion to its value narrowed the radius of profitable shipment. (Waylite, for example, which cost $120.00 a carload at the plant cost another $120.00 to ship 150 miles.) Wildcat steel and coal strikes late in the war years also reduced the production of lightweight aggregate.
By this time however, Allied forces were on the move all over the world, and the end of the war was in sight. As the Germans absorbed a series of devastating defeats and the Japanese pulled back into their home islands, concrete producers began to cast a hungry eye at the vast post-war building market, swollen by almost five years of frustrated demand.
Jack Freedman's reactions were typical. He recalls that "in 1944 I felt the war would be over soon and the demand for block in the Boston area would be immense. I ordered a Vibrapac and in May, 1945, ordered another. They were very hard to get, even though I had placed my order well ahead of time. But right after the war, everybody and his brother, it seemed were going into the block business."
And that's the way it was all over the nation. In 1945 the final year of the war the increase in capacity and production which had been reversed in 1942 to 1944, was again resumed. The 500 million concrete block manufactured in 1945 represented a near-hundred per cent increase over 1944, and production for 1946 almost doubled again. The post-war demand for concrete block was tremendous; the Federal housing program alone called for 425 million units.
61
Production expanded rapidly to meet this demand. Increased supplies of parts and the greater availability of labor enabled plants to return to multiple shift operations. So did the return of the equipment manufacturers to full production. The rush to get into the block business was stimulated by some wild success stories floating around the construction field. Tales of 20 to 50 percent returns on capital investment within one year were common. Many of these stories were circulated by fly-by-night equipment manufacturers who were making cheap, hand operated block machines. In Cleveland, for example, 20 small plants started up in a period of six months in 1946, about half of them using small hand machines, and the rest operating with ancient machinery. In Detroit, some old tamper block machines dating back to 1916 were actually returned to production.
Overcapacity and its constant companion, cutthroat competition became an instant problem, and the casualty rate among inexperienced block makers just back from the war was alarming. Even during the inflated war construction demands, there had always been ample capacity in the block industry; only labor and spare parts were lacking. There was also enough capacity to meet post-war demands, but before it got cranked up, there were hundreds of neophytes in the business and the plush post war market began to look as if it might turn into a price-cutting nightmare.
Largely because it was prepared for the tremendous post-war demand for building materials, the concrete masonry industry in 1946 was able to market a billion 8-in. equivalents, or twice the peak production in any previous year in its history. This output was equivalent to all the wall area represented by the combined production of concrete and clay masonry units in 1941.
So, by war's end, the block industry had come full cycle from apathy and lagging production, to wild optimism and burgeoning demand. But the optimism had, in itself, the seeds of its own destruction. The post-war market was a luscious plum; but it wouldn't and couldn't last forever.
As soldiers came home and a nation re-geared emotionally and physically to peace, the block industry was gearing for the strongest, wildest period of production and sales in its history.
62
These two plant views, taken late in World War 11, show the newest types of automatic vibrating block machines used during this period. Because machinery manufacturers were diverted into war production, it was extremely difficult to obtain block making equipment during the war years.
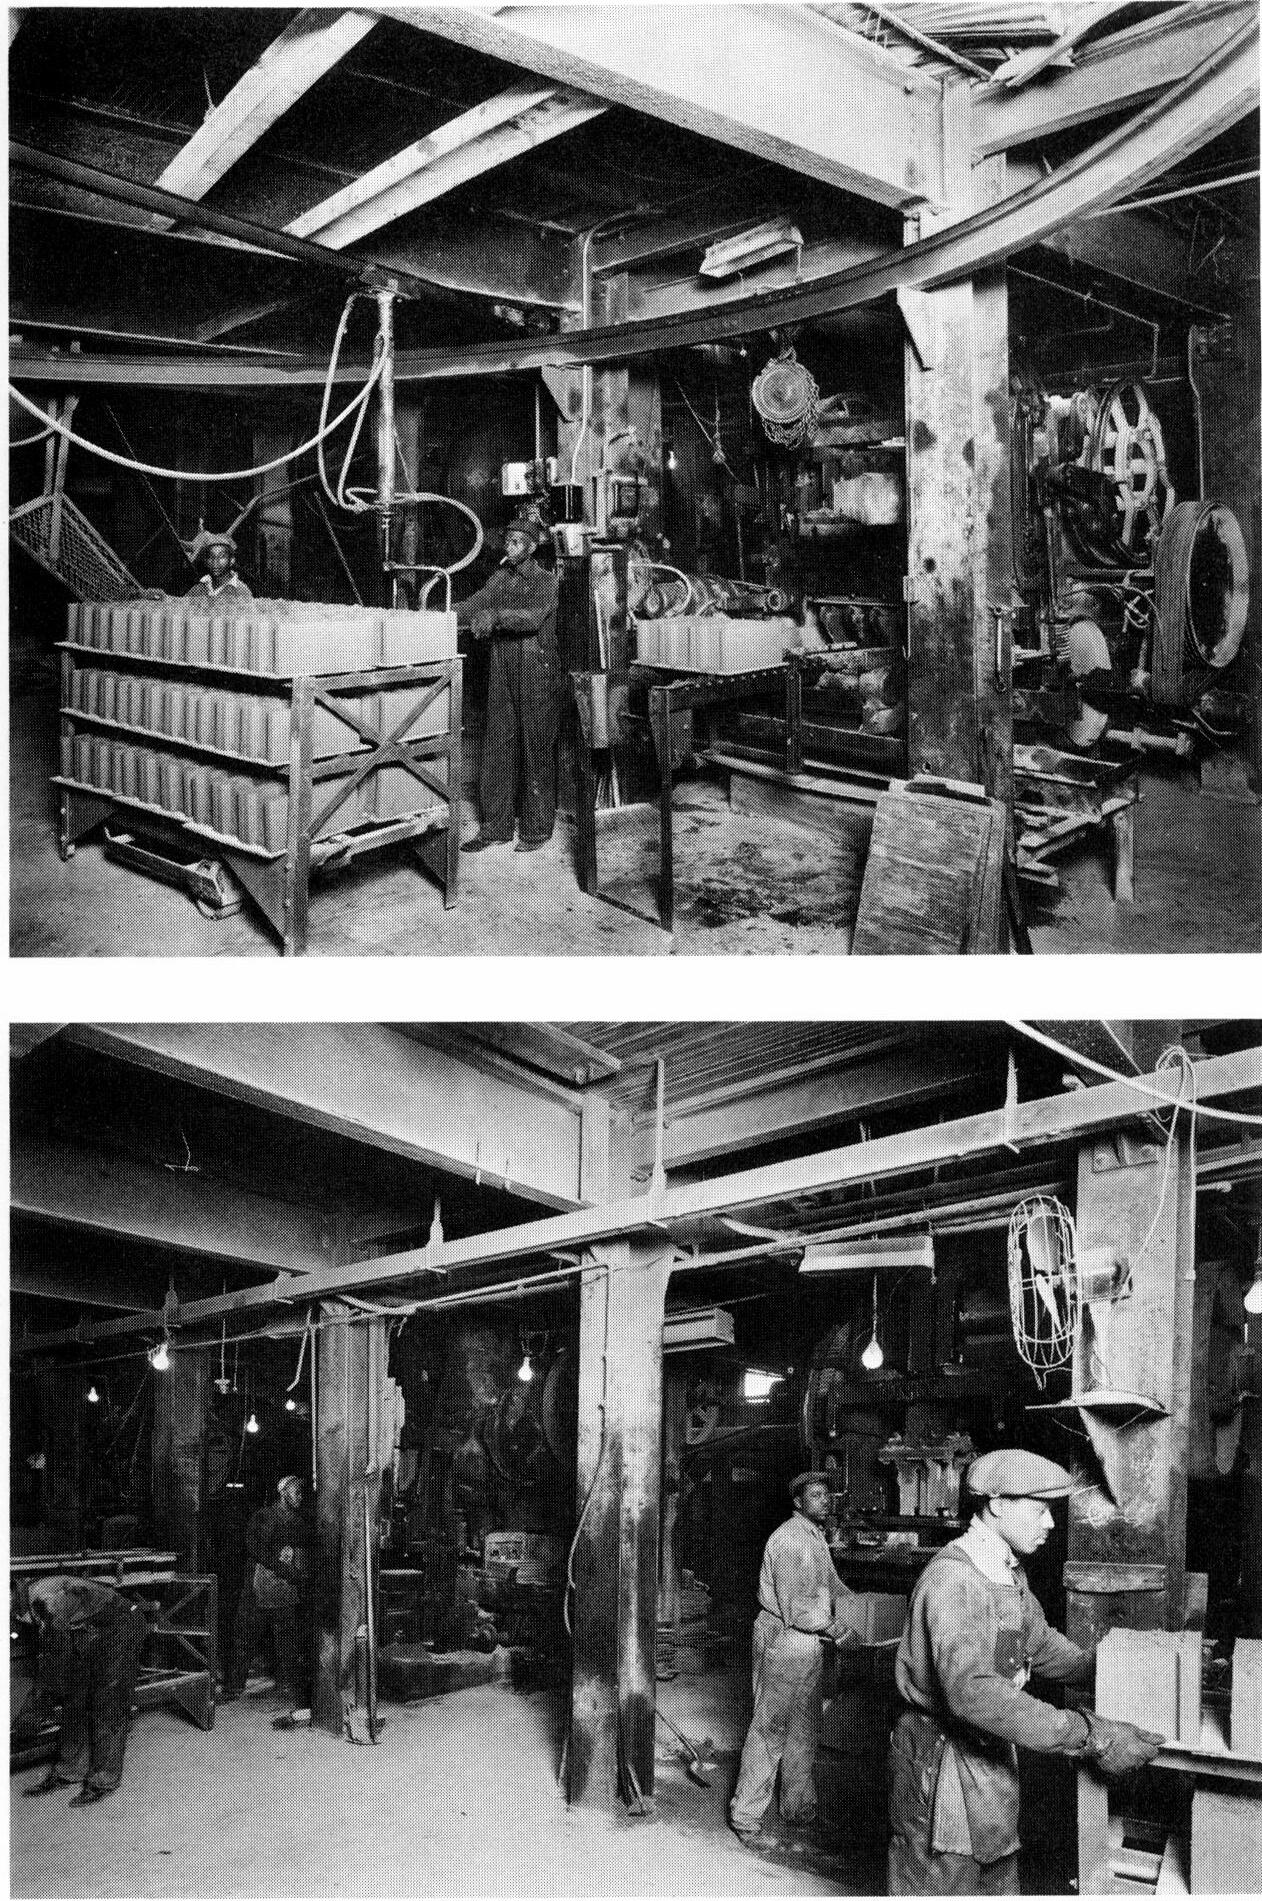
63
This
This shows how the yard of a modern block plant looked during World War II. Although the yard is still unpaved, the block is neatly palletized and delivered in modern trucks.
64
is typical of the special equipment used during the World War II years to haul block gravel from the pit to the manufacturing plant.
Figure#44
COST OF EQUIPMENT TO PRODUCE
20,000 8x8xl6 BLOCKS PER 18 HOUR OPERATING DAY*
MARCH, 1941
2- Super Vibrapac Plain Pallet Strippers with Power Offbearing Hoist $22,700.00
4- Attachments at $600.00 each 2,400.00
Note: Both Machines equipped for 8x8x16. One machine equipped for 4x8xl6 and 6x8x16
240 Ft. Besser Batch Mixers equipped with 25 H.P. Motors, VBelt Drives, Oil Retaining Gear Housings, Drum Grid Covers, Extension Hoppers and Water Meters. 4,954.00
2- Skip Loaders equipped with Geared Head Motor Drives 1,800.00
350 - Power Lift Truck Racks at $33.60 each $11,760.00
2- Power Lift Trucks at $2,770.00 each 5,540.00
7000 - 26-18-11 x a Steel Pallets at $1.15 each 8,050.00
2- Hand Lift Trucks at $300.00 each 600.00 25,804.00
TOTAL COST OF EQUIPMENT . . . . . . . . . . . . . . . . . . . . . . . . . $57,804.00
Note: Shown in plan, but not required for temporary Plant Extra for Hoppers, Elevators and Batchers $ 4,086.00 *Information supplied by Besser Mfg. Co., Alpena, Michigan
COST OF PRODUCTION
10,000 - 8x8xl6 CONCRETE BLOCKS March 31, 1941
(Equipment: Two Super Vibrapacs; one nine-hour shift) 4- Mixer and Aggregate Men 1- Pallet Man 2- Block Offbearers 1- Lift Truck Man (Inside) 1- Lift Truck Man (Outside) 1- Foreman 4- Yard Men 1- Mechanic 15 at $1.00 per hour Average $135.00
143 yards Aggregate at $1.50 215.00 400 sacks Cement at $.50 200.00
Repairs and Maintenance 20.00
Electric Power 20.00
Steam Curing 50.00
Taxes and Insurance 20.00
Administration Expense 50.00
Depreciation 50.00
Dismantling, shipping and Erecting 25.00
Cost of manufacturing 10,000 - 8x8xl6 units $785.00
Cost per unit $7.85
65 Figure#43
TYPICAL PROVISO OF OFFICE OF PRICE ADMINISTRATION FOR CONCRETE BLOCK INDUSTRY DURING WW II
Retail Sales Including Delivery A producer's maximum retail price for concrete blocks, delivered, shall be determined by adding the appropriate one of the following amounts, per block, depending on the size of the block and the location of the buyer, to the maximum retail f. o. b. price as determined under subsection (a) of this Section 3:
Amount which may be added, per block, for delivery
4 in. block 8 in. block 12 in. block Chimney block
For delivery to points within a radius of 10 miles of the producer's plant . . . . . . . . . . . . . . . . . . . . . . . . . . . .
For each additional 10 miles or fraction thereof, by which the point of delivery is located beyond a radius of ten miles of the producer's plant . . . . . . . . . . . . . . . . . . . . . . .
$.01½ $.02 $.03 $.05
$.00½ .01 .02 .03
66 Figure #46
The Space Age
1951 was a record year for concrete block. The output of 1.6 billion 8-inch equivalents was the largest ever, some 18 per cent over the previous year. In spite of material shortages and burgeoning transportation costs, lightweight aggregate continued to take over a rapidly growing share of this production. For the first time in 1951, more than half of the total output consisted of lightweight block.
There were other changes in the wind. For example, the concrete block industry began to look outside itself and find a small sense of social responsibility. In Alpena, Michigan, the Besser Company largest suppliers of block machinery donated a school for concrete technicians to the local community college. It still operates, one of the few schools like it in the world. The same year, NCMA began to sponsor the Thomas Noble Award a $500.00 cash prize for the year's most meritorious contribution to the production or promotion of concrete block. The NCMA also inaugurated in 1951 its "Home of Distinction" planning service. Members could obtain, at cost, a portfolio of perspectives and detailed working drawings on 16 attractive concrete masonry homes, designed by the architectural firm of Loree and Sirrine of Ann Arbor, Michigan.
"Available to NCMA members" became a meaningful phrase in the concrete block industry. Requests from non-members were handled with a form letter that said, tersely enough:
“According to a recent ruling by our Board of Directors, any promotional material we publish is available to members only. As you can understand, the cost of preparing and distributing such material is quite high and we believe you can appreciate why our members feel that this literature should be restricted to members only.
However, we hope you will consider this letter as a cordial invitation to become identified with other producers who comprise our membership, in which case you would be able to take advantage of the many activities of this Association.”
In case the subtleties of this message were missed, the NCMA had plenty of success stories to cite. Fairly typical was the Eastern block producer who was told through the NCMA's Washington office about the projected construction of 175 houses at a nearby air base. Forearmed, the producer contacted the architect,
67 VIII
worked with him from the inception of the project, and was finally awarded the purchase order on the entire job the largest single order his plant ever filled.
Through the early 50's, the housing boom carried concrete block production onward and upward. In Florida. for example, more than nine-tenths of all new construction was concrete and most of that was concrete block. And there was plenty of new construction. In 1954, more hotels and apartments were built in Florida than all the rest of the world combined.
In October, 1954, five members of the Expanded Shale Clay and Slate Institute decided to sponsor the design and construction of two lightweight concrete masonry houses as part of Operation Cue, Yucca Flat, Nevada, in preparation for the historic atomic blast to take place in 1955.
The 1,000 sq. ft. expanded shale concrete masonry houses were not "souped up" for this test. Walls were moderately reinforced with half inch steel rods vertically placed 32" apart, in accordance with the California building code. Horizontal reinforcing was in bond beams and lintels. Construction of room partitions was identical with outside walls. Roof was constructed of six-inch reinforced lightweight (expanded clay) concrete slabs. Foundation was a flat slab with a thickened edge which formed a beam around the perimieter.
The lightweight concrete houses on "Doomsday Drive," only seven eights of a mile from the tower on which the atomic device was mounted, were left standing after the blast. They suffered only slightly cracked walls and broken windows.
M. E. (Doc) Rinker of Palm Beach, Florida took over the reins of the NCMA in 1954, urging that "intelligent education of the architect, engineer and builder into the wide adaptability of concrete masonry, and assistance to masons and contractors in its use are fundamental responsibilities of the producer of concrete block." Outgoing president Sam Paturzo of Baltimore, Maryland, warned his associates about the danger of overproduction when the current building boom tapered off. And F. J. Straub surfaced at the convention to take a bow from the podium. He was introduced modestly as "the father of this industry" and made no effort to quarrel with the tale.
In 1955, the first NCMA state chapter was formed in Nebraska, where full compliance was reached with regulations established a year earlier by an NCMA committee on Local, State and Regional Associations. The NCMA also protested an effort by the Structural Clay Products Institute before the Federal Trade Commission to limit the use of the word "brick" to products whose composition is "primarily of clay" and whose ingredients are "fused together by heat."
Horrendous weather didn't prevent the 35th annual NCMA convention in Cleveland from being the second largest in history in attendance. Among other things, the assembled block producers heard an announcement
68
that Frederick W. Reinhold. president of Anchor Concrete Products, Inc, in Buffalo and a former president of the NCMA, had named the NCMA as beneficiary of a $15,000.00 life insurance policy, the money to be used for research appropriate to the needs of the time.
There were indications in 1956 that the post-war prosperity express was running out of fuel. Block production was down about 4 per cent as housing tailed off in spite of a record volume of construction overall. Two engineers were added to the NCMA research staff under R. E. Copeland, dividing their time between handling inquiries from members and exploring such industry problems as procedures for measuring block shrinkage, means of carbonating block artificially, and studies on mortar bond and high pressure steam curing. NCMA promotion under William Markert was venturing more heavily into national advertising and stepping up distribution of the bi-monthly Pictorial to potential customers of concrete block.
The block industry had no control over one of its principal problems in the late 1950's: the frequently critical shortage of portland cement. Only the shutdown of construction in northern climates during the winter made it possible for many block producers to obtain cement. Consequently they were operating at maximum capacity in the winter months to stockpile against cement shortages in the Summer and Fall. About the same time, the block industry got caught in the crossfire between two building trade unions, each seeking to push the other out of basement construction work. The anti-block union took out several ads showing a leaky block basement and calling it "second choice." This hit an especially touchy nerve because poured concrete was cutting deeply into the block foundation market.
But housing continued to be the bell weather of the block industry, and it turned back up after the small setback in 1956. U.S. News and World Report predicted a demand for 5.6 million new houses between 19561960 and suggested that new families of "war babies" would keep it booming indefinitely after that date, a prediction that proved to be over optimistic.
Visitors to the 1957 NCMA convention in St. Louis saw a new 16 mm film called "The Concrete Masonry Story", designed for showing by local block producers to architects, engineers and contractors as well as civic, fraternal and educational groups. The Concrete Industries Exposition attracted a new high of 130 exhibitors, and one of the featured speakers told the conventioneers:
"It is pretty well conceded that the housing market offers one of the greatest potentials for our industry. In many sections of the country, the average block producer enjoys a good residential foundation business. In many other areas, however, this market has been lost to poured concrete, so we can not call this market our own any longer. While above grade we are beginning to sell some slump block and split block for veneer purposes, the houses are still made principally of frame construction. PCA has spent a lot of money to promote housing with very little results. From our company's experience, we find that the only way we can
69
really promote housing is by sponsoring a model house with the large scale homebuilder or developer. There is a prospect of making our efforts worth-while by dealing with the builder of tracts of houses rather than the individual home owner."
A month before he succeeded Earl Peterson as NCMA president at the 1957 convention, Philip Paolella of Connecticut's Plasticrete Corp. was writing John Strandberg some searching questions.
"Is it not urgent," he asked, "that we endeavor to establish a means of getting closer to our membership? To date, we have little progress show regarding the Local, State and Regional Associations matter. Should this project be dropped? Or, should we further extend ourselves, possibly subsidizing initially, a few local offices for a trial period?"
In addition to membership problems, Pres. Paolella was handed two other major hot potatoes: what to do about a proposed new NCMA headquarters and how to handle the impending retirement of Executive Secretary Elmer Dienhart. The second was tied closely to the first since Dienhart approaching retirement age had indicated that he didn't care to leave Chicago at the same time the sentiment for moving the headquarters elsewhere was growing.
It had been clear for some years that the NCMA needed a laboratory and general office building. Accordingly, in 1956 the Association bought a five-acre tract in West Chicago for erection of a one-story building with 6,000 feet of laboratory space and 4,000 feet of office space for the headquarters staff.
Then came multiple complications. First, there were zoning and annexation problems that tailed off into a series of frustratingly deliberate hearings. While this was going on, sentiment for moving the office to Washington D.C. began to grow stronger. The Association already had a branch office there under Ted Leba. Why not, urged this group, consolidate that office with the NCMA headquarters in the nation's capital? Two primary reasons were offered: first, such a move would place NCMA officialdom close to the source of federal power and regulatory bodies and government purchasing; and, second, the Washington area was less expensive than Chicago as a base of operations.
While the West Chicago hearings dragged on, the Washington group prevailed and the decision was made by the NCMA directors to move Association headquarters to the nation's capital. During the time this decision was being made, Elmer Dienhart NCMA's first full-time executive officer retired. Director of Engineering R. E. Copeland didn't want to make the move, and he was changed in 1959 to a consulting status with the assignment of writing a new technical design manual. At the other end of the geographical spectrum, NCMA's Washington man, Ted Leba, left in 1958 to set up a consulting practice. And so the move was made in mid-summer of 1959 with a largely revamped staff.
70
The first order of business was, of course, the appointment of a new Executive Secretary. A committee set up to screen candidates reported, in part, in mid-1957:
We naturally gave first consideration to the members of the Association, staff, particularly Messrs. Copeland, Markert and Leba, in charge of our three principal departments engineering, promotion and the Washington office. There has been no question in our minds that all three of these men are functioning well in the departments of which they have charge. At the same time, we discussed at length the advisability of considering the employment of a man not now employed by the Association especially in view of the fact that we have the impression that a considerable sentiment exists among members of the Board of Directors to engage the services of some individual who hasspecializedinorganization work, such as membership. The Board of Directors feels that the principal task facing the Association at this time is to increase the regular membership which now stands at approximately 550 companies.
At our third meeting, we invited six candidates to come to Chicago for a personal interview. Strangely enough, only two presented themselves. These men made a strong impression upon the committee. After due consideration the members feel that Walter Underwood would probably best fill the qualifications, especially in view of the fact that he has had wide experience in membership promotion.
And so it was done. In May, 1957, Walter W. Underwood became the first Executive Director the title chosen by the committee to replace Executive Secretary of the NCMA. A graduate of the Princeton University School of Military Government, Underwood served as a Navy officer during World War II, then joined the Houston (Texas) Chamber of Commerce. He headed up membership departments in Chambers of Commerce in Sacramento, California, and Portland, Oregon before moving up as western states National Affairs Advisor, then California district manager for the U.S. Chamber. Immediately prior to accepting the chief executive post for NCMA, Underwood spent three years directing a membership expansion program for the National Association of Home Builders.
The new Director of Engineering came from the NCMA ranks. Henry Toennies had joined the Association in 1954 from a post as laboratory chief for a large Ohio architectural and engineering firm. When Copeland decided not to make the move East, Toennies joined Walter Underwood and Bill Markert (who departed NCMA shortly thereafter and later headed up a New England block group) as the nucleus of the new administrative team.
The breaking-in period was complicated by logistical problems. After settling in Washington D.C., NCMA bought a Georgetown property on which to build, only to run into nagging parking, architectural and zoning problems that sent them fleeing finally in 1963 to a commercial office building in Arlington, Virginia, which was about twenty minutes driving time from a rented lab facility in Silver Spring, Maryland.
71
Between and around moves, Walter Underwood put into execution sweeping changes in NCMA's organization structure. In order to attain "optimum practical membership" with a "balanced work program against a maximum practical budget," Underwood facilitated communication between the national organization and its producer members by:
l. Developing leadership at local and regional levels;
2. Establishing field programs at local and regional levels; and
3. Conducting local and regional meetings to reassess the work and program of the NCMA.
The first step in 1958 was to divide the country into six regions. Each region elected one or more directors and a regional vice-president. An Executive Committee would act on policy matters between board meetings, and a Senior Council would advise the president on long range programs. Working with the executive director, the regional vice president would explain and implement the efforts of the home office staff and "sell" NCMA programs to the members in his region through frequent area meetings. The regional set-up would also expedite the acceptance of local associations into affiliation with NCMA with full reciprocity of membership.
Thus did Walter Underwood while beset with personnel and location problems change the face of the NCMA.
The move to Washington further severed another prop that had long supported at first visibly, more recently only philosophically the structure of NCMA. This was the close relationship with the Portland Cement Association. Since the end of World War II, it had been more implied than real but the PCA's national headquarters in Chicago had always been close at hand. With the NCMA in Washington, this was no longer true.
The complete severance also represented a growing philosophical schism in the care and feeding of members. PCA, with virtually the whole cement industry in its membership, made its information and materials rather freely available to all concrete block plants. The NCMA, struggling to persuade a larger segment of the block industry to support Association activities, wanted to be more hard-nosed about refusing help and materials to non-members. And so the lines of communication between the two Associations became more and more tenuous. Several joint research studies continued (the freeze-thaw resistance of block, for example) and PCA help was usually available when the NCMA asked for it. "But," as one NCMA official said, "we're like a South American country getting aid from the United States. We tell the PCA we don't think they're doing enough on block. And they say they're spending more than we are, and we go round and around."
Late in 1957, a Chicago patent attorney notified the NCMA that its application for a trademark of its name had been officially approved by the federal government. A few months later, delegates to the NCMA convention heard Frank Lloyd Wright discuss his love affair with concrete block; they also heard another speaker warn
72
that high pressure promotion by block machine manufacturers was bringing a new influx of small, ill-equipped producers into the business whose main contribution would likely be a cycle of price cutting.
About the same time, Phil Paolella, the chairman of the Senior Council (renamed the Past Presidents' Council) was issuing its first communiqué, which suggested, in part:
It seems of extreme importance that we try to guide or lead the direction into which our industry is heading. During the past fifty years, our growth curve has been upward. Now it seems to be leveling off. We must ask ourselves "Will it rise again or what will be the status of our industry five years from today and ten years from today?" We must give special consideration to these questions in light of the fact that glass and panel construction are increasing in popularity. Prefabricated wood and metal buildings can be made available on quite simple and easy terns on arrangements that cannot help but prove attractive to prospective owners of commercial buildings. The commercial, industrial and institutional markets are still the largest users of concrete masonry. Poured concrete has not yet completely overcome concrete masonry for foundation use. Many of our member companies still enjoy a good foundation business. It is a fact, however, that poured concrete basements are taking over city after city, because of cost and because of the unavailability of masons who are desirous of doing foundation work. The metal, wood and plastics industries are spending millions of dollars each year for research and more millions for promotion. Our industry is composed of more than 2.000 relatively small companies that are doing practically no research and little promotion, with just a few exceptions. How seriously willthese factors affect our future markets?
A segment of the block industry still wasn't concerned enough about these problems to join the NCMA. By mid 1958, the 600 regular and associate members represented about 50 per cent of the industry's total productive capacity. The strongest representation was in the South, Midwest and East, and the weakest showing was in the Far West and the Plains states. Of the 45 regular international members, 31 were from Canada.
This same disinclination for cooperative action was to a large degree responsible for the almost total lack of progress in dealing with one of the industry's oldest and most nagging problems: price-cutting. An anonymous producer speaking out in Concrete Products Magazine in 1962, pretty well summed up the views of responsible industry representatives when he said: "In this business, the supply of firms exceeds the demand for the products they manufacture . . . and this certainly is one of the contributing factors that causes price wars. . . . When a firm drops well below the going market price of other producers in the territory, this is an attempt to take someone's business away. And special deals to certain customers are another telltale sign of an unethical procedure that could blossom into a price war.
73
"We once calculated that if we were to cut our prices by 3 percent, we'd have to increase our sales volume by nearly 14 percent to show the same profit; a 10 percent cut would mean a 67 percent sales increase, and a 20 percent cut would call for a sales step-up of around 400 percent. So we merely pay more attention to our own business than to the other fellow's. We always try to give good service and the best quality not just in times of a price war. This is why our business hasn't suffered. I'd rate price in third place, behind both service and quality."
Price cutting was an old problem. Some of NCMA's newer problems in the early '60's were more exotic and more subtle. The regional restructuring of membership for example, was making painfully slow inroads into a problem that had long been troubling but seldom articulated: the tendency of a fairly small group of nationally oriented and strongly motivated producers to pass the direction of the NCMA back and forth among themselves. This was a source of irritation to members and prospective members, and there was strong feeling that a greater democratization of the NCMA was needed.
The regional organizations opposed by a number of the old-line members was a move in this direction. But while this was tending to open up the top echelons of NCMA, some of the other new policies had an opposite effect. There was, for example, a strong thrust to close out non-members from even peripheral benefit from NCMA activities. This was one reason PCA with a much freer distribution policy-was moved completely outside the NCMA operation, a separation that helped inspire NCMA to broaden the base of its own publications and open the pages of one to national advertising (a move the trade magazines didn't appreciate). The tough attitude toward non-members, however, reacted negatively on some of the state affiliates, and there was a good deal of confusion as to the nature of the roles played by NCMA as opposed to the state Associations.
Consequently, there was a general threshing around in the early 1960's to come up with meaningful industry-wide programs that would offer something to everyone. The Q-block program, for example in which producers nationwide were urged to emphasize quality never really caught fire, never captured quite enough imagination.
In the promotion end was a growing list of NCMA publications. Concrete Masonry Pictorial was started in 1944 as an occasional 8-page black-and-white picture book designed to illustrate the "postwar markets for concrete masonry." By the early 1960's, it was a monthly, four times that size, in full color, and was being sold to producers for redistribution to a list of some 40,000 potential customers for concrete block. C/M Magazine, however, was not faring as well. Designed in 1961 as an external trade book, it didn't attract enough advertising to pay the bills. So in 1962, the name was changed to C/M News, the format was changed to tabloid, and the losses were cut considerably.
74
The NCMA laboratory had been one of the early casualties of the headquarters building plan that failed, both in Illinois and Washington. A small lab functioned briefly in connection with the office at its first Washington location; when the office was moved, the lab was set up for several years in separate quarters in Silver Spring. It was then moved to its present location in the midst of a small industrial complex in Alexandria in July, 1966.
During the same period, the NCMA engineering emphasis went through a similar transition. Before 1960, the lion's share of engineering effort was expended on manufacturing improvements which is precisely the way the NCMA members wanted it. The most spectacular post-war engineering achievements came in the growing knowledge and use of autoclaving. NCMA engineers made two major studies of autoclaving that were of considerable help in counseling members how and if they should follow this route. There were also a number of studies (some in tandem with PCA scientists who first discovered it) on carbonation that resulted, finally, in a 1961 research report that won international recognition and a Wasson Medal from the American Concrete Institute for Director of Engineering Henry Toennies.
Today, the main thrust of the NCMA engineers as with their promotion associates is toward market expansion getting as much block used in all construction as possible. Consequently a great deal of engineering time is now being spent on multi-story load bearing walls of concrete block. In conjunction with this work, the NCMA in 1969 offers computerized solutions to specific high-rise design problems in concrete block. Customers of NCMA members can send their problems to the Association; within a few hours they are fed to the computer by NCMA specialists and the answer fired back.
The evolution of all these activities was positive and generally helpful to the industry. But they also seemed too little and often too late slightly out of synchronization with the industry and the world as it was then, rather than as it used to be. There were substantial changes taking place in the block industry in the 1960's, and the changes seemed to be outrunning the ability of the Association to regear for them.
What were some of these changes?
First, there was the headlong run to automation and a growing amount of super-sophisticated plant equipment;
The accelerating trend of an industry changing from many small manufacturers with limited investment to a relatively few large manufacturers with considerable resources; obviously, the trade association needs of large manufacturers was different, and some felt the NCMA was no longer very responsive to them;
75
The move of the NCMA to Washington to be close to the government agencies that provided acceptance for the product turned out to be a misplaced emphasis. Acceptance was no longer the problem; concrete block was accepted. The need was to sell it in a drastically changing construction market.
Thus there was a restlessness in the NCMA and in the block industry that was well reflected in a 1965 guest editorial in Concrete Products Magazine by J. W. Kingery, executive vice-president of Concrete Manufacturing Co. in Atlanta, Ga. Said Kingery, in part: "Too many of us and for too long have simply mailed in our dues and turned over the responsibility and work of running NCMA to someone else. It has not been doing the job for us because we haven't cared enough to demand better programs."
The same restlessness was reflected in NCMA membership figures. The gradual drop in membership through the early 1960's began to turn precipitous in 1966. Construction was showing the same ambivalence during this period, with solid increases in commercial and public construction played off against erratic upsand-downs in the residential sector.
Not everyone agreed with these criticisms of the NCMA, and even the critics were quite willing to concede considerable progress that included an effective, comprehensive promotion program, a constantly improving Pictorial, and a number of pertinent and far-reaching engineering developments. The malaise was more one of changing times and conditions, and obviously a new program and a new dedication was required to check the slipping membership and excite new members.
Consequently, at midyear in 1967, more than a hundred members of NCMA from all over the United States devoted nearly a week's time from busy schedules to meet in Washington, D.C. and explore means of improving the NCMA financial position. It was decided to request voluntary contributions from those firms that could afford them, and some $16,000 was pledged before the meeting ended. The goal was $75,000, a figure designed to meet current financial needs and set the NCMA on a new course of service to its members. Those gathered in Washington decided to call their program Operation Commitment and that's what it turned out to be: a commitment to the future of the industry and the Association that served it.
The NCMA president in 1968, J. W. Kingery, put it this way: "NCMA is on the move. Meaningful programs have been formulated with two thoughts in mind: the most program for the most members and more substantial profit for our members." To prove it meant business, the Board of Directors of the NCMA unanimously approved an unprecedented $800,000 budget for the following year, 1969. "We want our program," concluded Kingery, "to be so great that no one can afford not to belong to NCMA."
76
While these high-level policy changes were taking place, two block industry pioneers passed from the scene. F. J. Straub whose greatest joy in his last years was reminiscing past glories with associates, young and old died in 1966. A few months later, the NCMA's first Executive Secretary, Elmer Dienhart, succumbed to a heart attack in his home in Des Moines, Iowa.
Then, in the midst of Operation Commitment, came another major change. Executive Director Walter Underwood was offered a post as consultant to the Republican National Committee and requested early retirement from the NCMA. He departed in June, 1968 with a solid record of accomplishment that included a doubling of NCMA income, the establishment of a new NCMA office and laboratory, the development of a complete national-local marketing service for members, the establishment of C/M NEWS, and the founding of the NCMA New England Division. He also increased the NCMA literature list from 75 to 566 items and the total distribution from about 100,000 to almost 750,000 annually.
His successor was a man with a solid reputation and record of accomplishment in a field that NCMA officials had decided should constitute the major thrust of Association activities: marketing, merchandising and the expansion of product use. Paul Lenchuk had served for 14 years as operating head of one of the nation's strongest and most effective state Associations, the Florida Concrete and Products Association. NCMA president Kingery called him "the very best possible person to act as executive director and to lead NCMA in the years to come." The Florida Association included the largest number of producers and greatest block production of any state group in the nation. During his long stay there, Lenchuk innovated a complete Educational and Management Program, a successful joint approach to union problems, a landmark campaign for maintaining good labor relations within the Florida concrete industries, a massive million-dollar-a-year insurance program for members, many promotional programs including one at the New York World's Fair, and a low-cost housing program designed to attract the support of savings and loan institutions for concrete block.
Lenchuk's first order of business at NCMA in June of 1968 was to bulwark a sagging and dispirited membership. He asked them only to delay decisions, at first, while the NCMA sought to correct some of the inequities that were driving members away. One of the efforts in this direction was to stabilize the dues base. Once based on production figures, it had been changed to the number of mold boxes because production figures weren't being reported. But the mold box wasn't working any better. Dozens of producers were being assessed dues on the basis of long departed one-at-a-time machines. They were told, politely, that their dues would now have to reflect their actual number of mold boxes. A few dropped out; most paid up.
With this fence mended, Lenchuk turned his attention to two other areas of NCMA strength-building: the attraction of new members and the provision of income-producing auxiliary services. The latter fell into four main categories:
77
Educational seminars for technicians, salesmen, foremen, supervisors and top management on a variety of subjects, for which enrollees paid a tuition fee;
Updating literature particularly construction manuals and promoting its sale and distribution among members;
The production of packaged programs both technical and marketing for a fee for state associations, groups of members or even individual member companies;
Promotion of the Concrete Industries Exposition in tandem with the NCMA annual meeting.
Attracting old members to return to the fold and soliciting new members was a common and different problem. Obviously it could only be done by putting together an Association program that would not only prove attractive but would also rebuild slipping confidence in the necessary functions performed by the NCMA. Called the New Look, the program was announced in the Summer of 1968, financed by the largest NCMA budget in history, it represented in very tangible terms the new NCMA philosophy subtle but important of changing emphasis from promotion to marketing. There would be no more across-the-board efforts; rather the NCMA would take dead aim on specific types of construction where it felt that concrete block's share of the market could be increased.
All of this was explained in a mailing brochure sent out to the block industry in the summer of 1968. Promotion programs were to focus on two market areas small commercial and industrial buildings and multi-storied loadbearing structures in 1969. Education and training programs were to be offered in autoclaving, block making, sales, and top management techniques. Research was to be directed toward developing a systems approach to construction with concrete masonry, aimed primarily at making further inroads in the $5 billion housing program of the U.S. Housing and Urban Development Agency. And Engineering would concentrate on testing of concrete block walls, development of information on the flexural strength of reinforced concrete masonry walls, and investigation of more economical ways of palletizing and pre-packaging concrete masonry units.
By mid-1969, more than half of the lost members had been recouped and the trend was definitely up. Less than half of the financing for the NCMA's expanded programs of service was coming from dues; the balance came from members taking steadily increasing advantage of the new services. NCMA was doing basic market research, then turning this information over to its members with the advice that they stop selling units and turn, instead, to an understanding of how building materials are selected and bought for a particular type of structure then take dead aim on that specific market. "We were losing markets without attacking the root of the problem," said one advocate of this new approach. "We were still selling block instead of markets."
78
And so NCMA turns a corner and heads into its second, fifty years with a new excitement, new dedication, new growth and a new and expanding base of support.
The end of that new turn is obscured in the distance. But the immediate path is brightly lit, and the signposts can be read clearly.
Says Paul Lenchuk: "We want members to look at their investment in NCMA, to look at their own sales, and then be able to see a direct return on their investment because of membership in the NCMA."
At the mid year meeting of the Board of Directors in 1969, the following resolution was passed:
"The Executive Committee of NCMA at a meeting held August 19, 1969, in Toronto, Canada, has reviewed in detail the operations of the association for the past 12 months. This group desires to go on record as warmly thanking the Executive Director, Paul Lenchuk, and commending him for excellent service as a leader, manager, organizer, and above all, as a doer. His tremendous abilities have made NCMA a dynamic organization."
The modern, high-speed block machine pictured here is entirely automatic and can produce up to 20,000 8 x 8 x 16" equivalents in a ten hour day. These machines began appearing in North American block plants in the early 1960's.
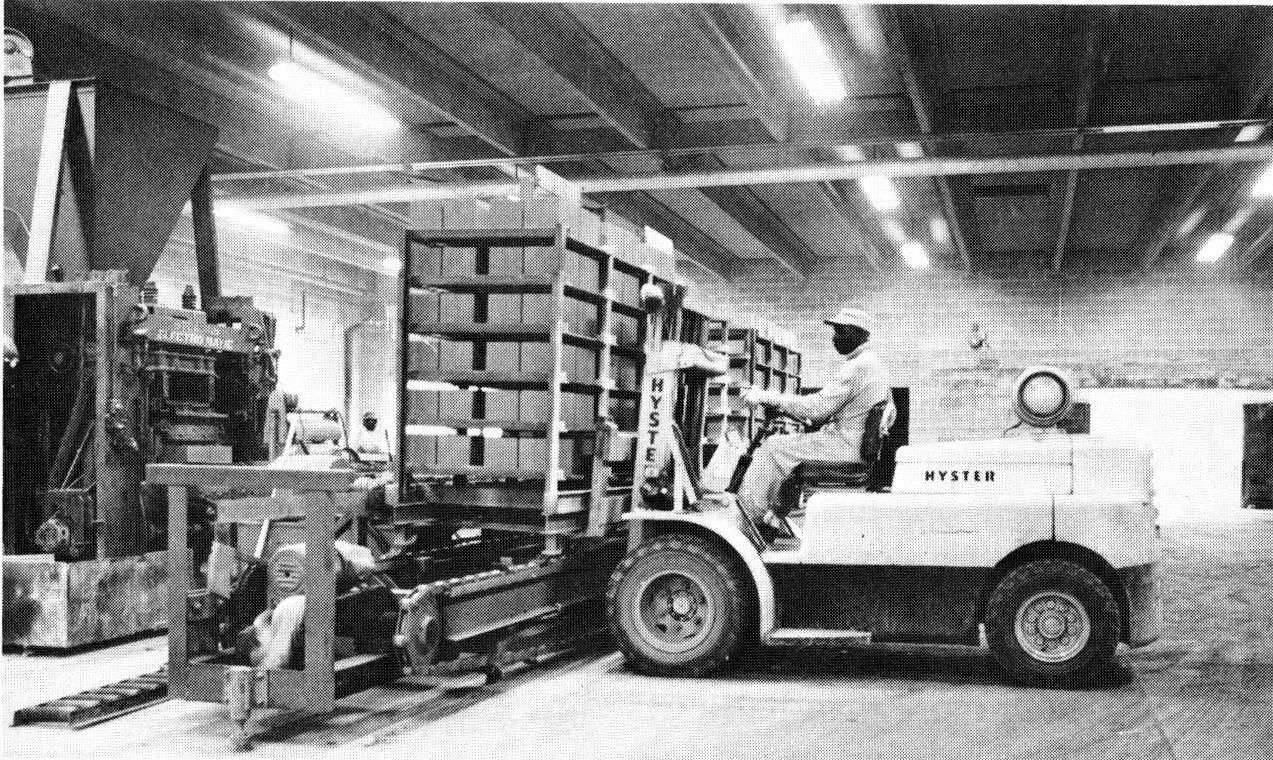
79
Pictured here is the sort of modern laboratory now appearing in moreand-more large, automated concrete block plants. This example is the Texcrete central research laboratory in Dallas. A chemist uses a stereoscope to examine the physical structure of a product sample.
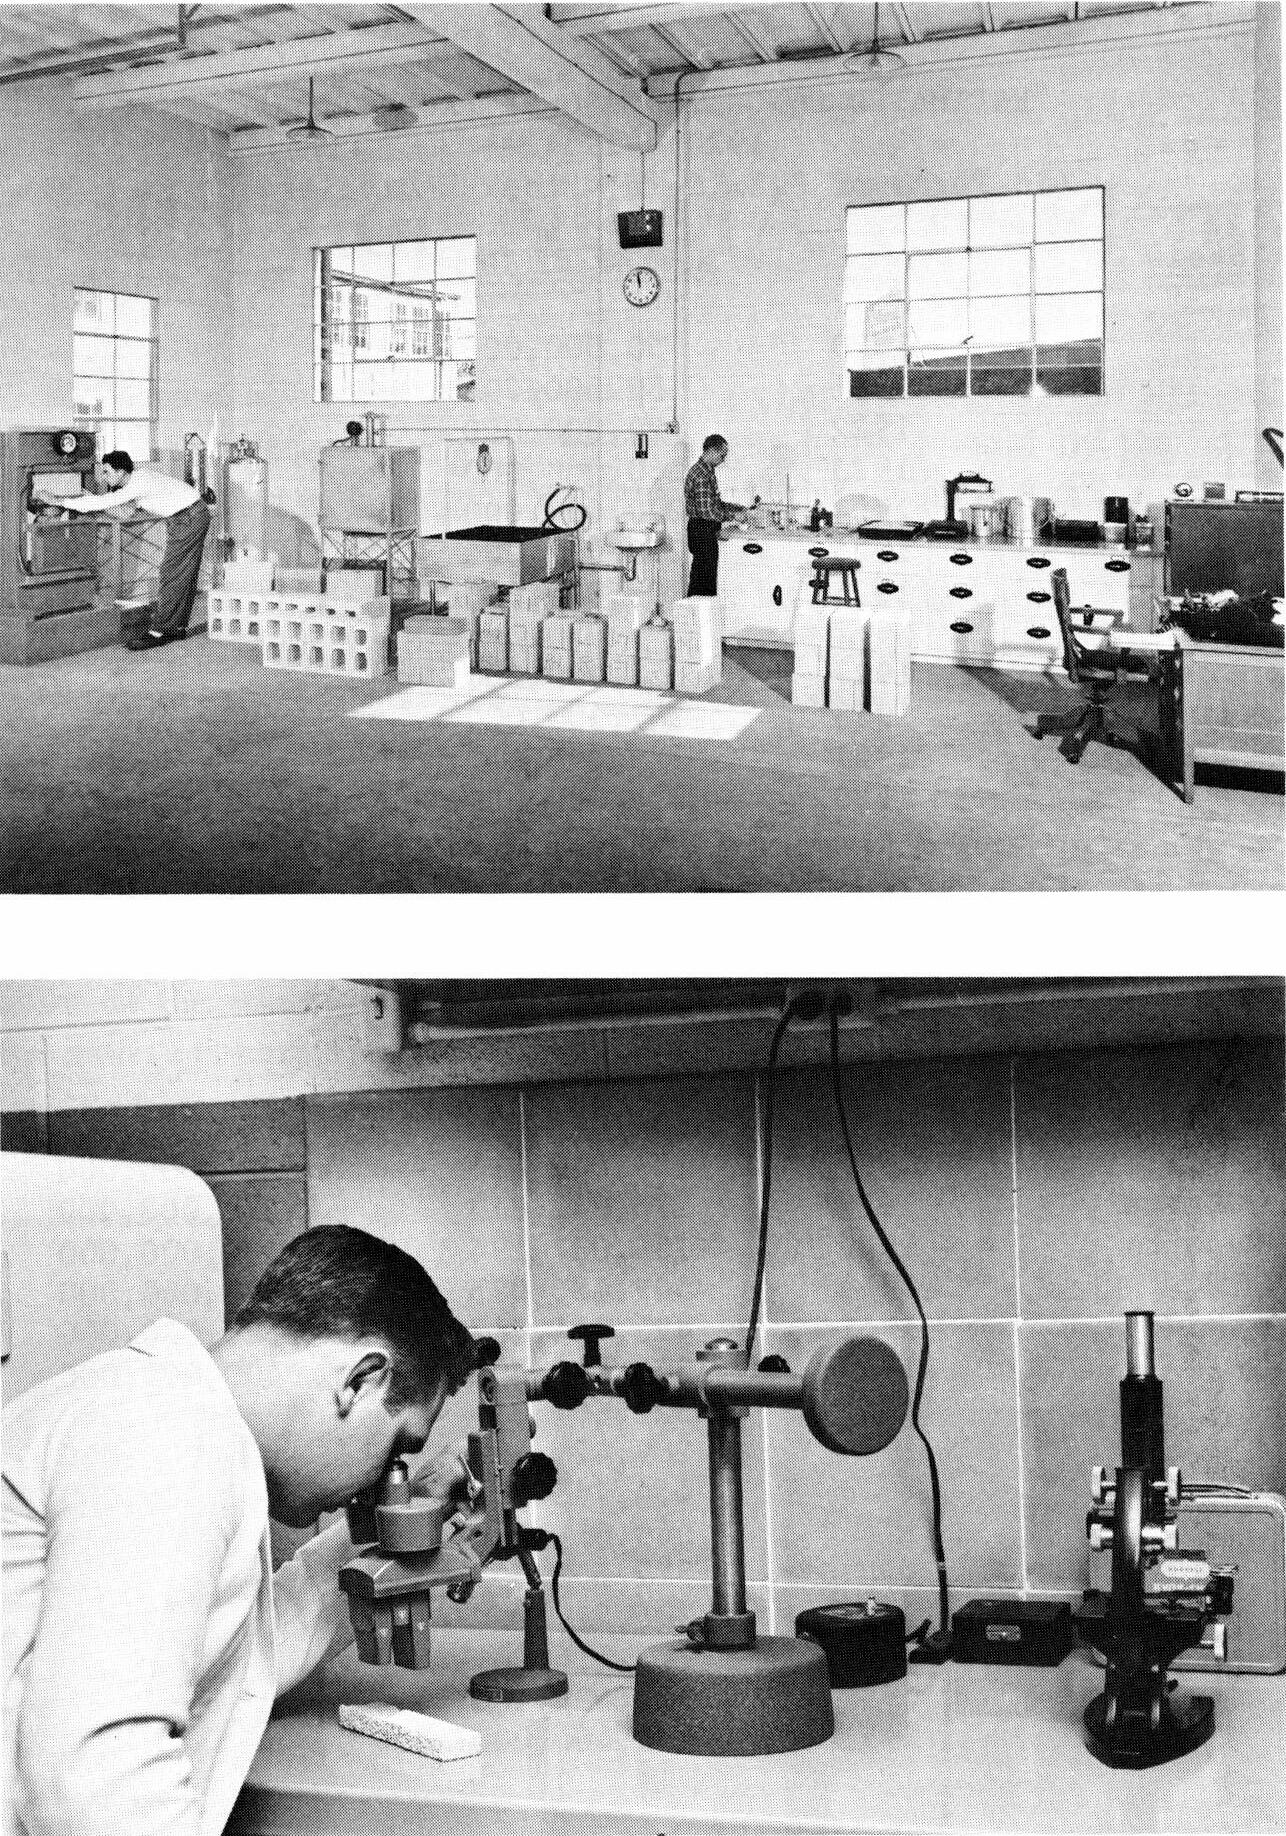
80
ESTIMATED CONCRETE MASONRY PRODUCTION 1920 - 1951 (In Terms of 8x8x16-in. Block Equivalent)
Basis Year Number of Units 1920 50,000,000 1921 80,000,000 1922 120,000,000
Estimated 1923 160,000,000 1924 200,000,000 1925 250,000,000 1926 300,000,000
Concrete Masonry 1927 353,000,000 Manufacturers 1928 387,000,000 Reports 1929 322,000,000 1930 210,000,000 1931 175,000,000 1932 65,000,000 Estimated 1933 50,000,000 1934 50,000,000 1935 100,000,000 1936 124,900,000 *150,000,000
PCA District 1937 171,882,015 *205,000,000 Office 1938 175,842,813 *210,000,000 Reports 1939 234,037,296 *280,:00,000 1940 309,488,075 *370,000,000 1941 423,774,217 *500,000,000 1942 340,841,391 *400,000,000 1943 322,667,065 *380,000,000 1944 289,425,435 *340,000,000 1945 454,765,300 *540,000,000 1946 1,040,317,000 1947 1,322,598,000 1948 1,396,296,000 1949 1,120,516,000(a) 1950 1,325,430,000(a) 1951 1,463,464,000(a)
*Estimated Total Production (a)Plants of 500,000 units or more annual capacity
81 Figure #47
Gallery of NCMA Presidents
An organization can almost always be characterized by the strength, dedication, foresight and intelligence of its leaders andbythatstandard, the National Concrete Masonry Association measures up exceedingly well, indeed.

Over the first 50 years of its life, the NCMA was able to draw on the talents and skills of the top men in the industry it represents, and without question this is why it has not only survived but gained strength and stature over those years.
Pictured on the following pages are the men who have led the NCMA since its birth in 1920. Each one has left his individual mark on the organization. All of them merit the thanks of their own and allied industries for the time and dedication they have devoted to the improvement of the trade association and the products it represents serving the field of concrete masonry.

82 IX
Benjamin Wilk Dan F. Servey 1933-35 1936-37

82

83

84

85
LightweightAggregates
About 2,000 years ago, the Romans used lightweight aggregate to reduce dead weight in the construction of their great domes in the Pantheon and the immense public baths in Rome among other distinguished public buildings. The aggregate was pumice, and fragments as large as six inches in diameter have been found in some of the Roman ruins.
Little is known of the use of lightweight aggregate from that time until shortly after the middle of the 19th century, when pumice concrete appeared in the Nette and Brohl Valleys in Germany. This pumice aggregate was obtained from local deposits, and the concrete proved so satisfactory that its use for lightweight construction began to emigrate slowly into other European countries.
In spite of these early stirrings, however, it was not until the end of World War II that anything more than sporadic attempts were made to manufacture lightweight aggregates. Before that time, the trend was almost totally directed toward the use of cinders of coal burning furnaces and the slags of various metallurgical operations. Important tonnages of such products were used in making concrete block for several decades prior to World War II.
Why did the widespread use of lightweight aggregates come about so recently in view of their obvious advantages and the length of time since their use in concrete? Some of the reasons apparently arise from the extra cost and necessity of additional storage bins and facilities for handling the required grades of lightweight aggregates. But mainly the answers appear to lie in changing construction needs and demands.
The need for lightweight building materials was created in the latter part of the nineteenth century by a radical change in building design concepts. Dead load or structural weight was transferred from thick, heavy, loadbearing walls to a load carrying framework of beams and columns with thin walls. This new design was brought about by the introduction of structural steel, followed by reinforced concrete and structural concrete as materials for the erection of the load-supporting frame. The new materials and methods of construction made possible the erection of skyscrapers and the building of bridges with long spans, and made feasible additions of one or more floors to existing buildings.
86 X
As size and design of the load-bearing framework are controlled chiefly by dead load, the natural result was a search for light-weight materials to use in partitions, floors, and exterior walls. Since these thin walls created problems of heat and sound insulation, building materials that possessed good heat and soundinsulating properties in addition to light weight were objects of extensive research. One group of materials developed to fill this need were lightweight concretes.
Although the advantages of lightweight aggregates were evident from the first skyscrapers, there was a transition stage between the old bearing wall and modern skeleton-frame types of building. As a result, it was not until the decade of the 1920's that the new lightweight concretes were recognized and used more extensively in the erection of large, nonresidential buildings. From this type of construction, lightweightaggregate concretes entered fields of residential and small nonresidential buildings, where the weight of each concrete block was reduced sufficiently to enable one man to handle it easily.
Before the Depression virtually halted construction in the early 1930's, lightweight aggregates except for Haydite which was introduced in 1923 consisted almost entirely of cinders. Then several other processed aggregates began emerging as important factors in those markets where supplies were available. Pottsco later renamed Celocrete was introduced about 1930; it was ordinary blast furnace slag, water-cooled at a carefully regulated temperature. Two years later came Waylite a "molten slag treated in a centrifuge in an atmosphere of stream, causing it to expand and thereby creating material of lightweight impregnated with non-communicating cells." This period also saw the introduction of Superock and the continued growth of Haydite which was being manufactured in eight plants by 1939. Several other processed aggregates were in the experimental stage at this time, and only occasional local use was made of them.
The strong revival of the building industry after the Depression was accompanied by greatly increased demand for all types of lightweight commercial aggregates for use in precast masonry units. Although cinders continued to prevail, principally by reason of widespread availability and low price, other lightweight aggregates both processed and natural began closing the gap.
Today, when almost 75 per cent of all aggregates used in concrete block in the United States are lightweight, the raw materials most commonly used can be placed in three general groups:
1.Natural Aggregates
Vesicular volcanic materials are the principal natural lightweight aggregates. Of these, pumice is the most important, although scoria, cinders, breccia, and tuff also are suitable for use as aggregate. Other lightweight substances that are suitable in their naturalform include diatomite and anthracite.
2.By-Product Aggregates
87
The most important by-product lightweight aggregates are aircooled slags and coal cinders. Coke breeze, the fine screenings obtained in sizing metallurgical and household coke, is also included in this group. So is sawdust, which has had only limited use in the United States.
The physical characteristics are more important than the chemical constituents in making cinders a satisfactory concrete aggregate. These characteristics include relative quantities of coal, coke, clinkers, and fine materials in the cinders plus the strength of coarse particles. Chemical determinations include combustible sulfide, and sulfate content. Although these combustibles have surprisingly small influence on quality, it is still generally true that suitability of the cinders for aggregate decreases as the combustibles increase. In the United States, specifications of the Underwriters' Laboratories limit the average combustible content of mixed fine and coarse cinders for manufacturing concrete block to not more than 35 percent by weight of the dry, mixed aggregates. Although anthracite cinders differ somewhat in physical characteristics from those obtained by burning bituminous coal, both are about equally suitable for concrete.
3. Processed Aggregate
Processed or manufactured lightweight aggregates are those obtained by treating raw materials to attain desired properties in products designed primarily for use as concrete aggregate. Widely varied types of patented manufacturing processes are employed. The aggregates belonging to this group have shown considerable growth in use in recent years and are divided into two main classes: expanded shales and clays, slates and expanded slags.
All expanded shale, clay, andslate aggregates are made by the same basic process, which essentially is the rapid elevation of the temperature of a prepared raw material to a point between its incipient and complete vitrification temperatures. In this temperature range, which is reached just before discharge from the kiln, the shale, slate or clay softens, becomes sticky, and tends to trap evolved gases. The material is discharged in this condition and cooled rapidly to retain the cellular structure.
Specially processed or expanded slags are made by treating molten blast-furnace slags with controlled quantities of water. Too much water produces granulated slag, which is not strong enough for use as aggregate, and not enough water increases the weight of the product. Techniques of manufacture are patented and differ widely as some slags are expanded in pits dug in the ground, while others are made in intricate machines. The expanded slags exhibit all the desirable properties common to lightweight aggregates and gave a pleasing light color that appeals to the manufacturer and buyer of concrete block.
Serious shortages of cinders and processed slags in recent years have provided sufficient incentive in many localities to process other available raw materials for the direct production of lightweight aggregates usually naturally bloating or expanding clays, slates and shales that have been crushed, screened, graded and marketed
88
under special trade names. In addition to the clays, slates, and shales, certain types of volcanic ash and perlite, vermiculite, diatemite, slates, and various other materials have been successfully used.
The combined water that occurs within the molecular structure of the perlites and vermiculites has been fairly well established as the constituent causing the expansion of those materials. This combined water is tightly bound and is released only at the higher temperatures under conditions that cause destruction of the original compact mineral form. However, it is also widely accepted that the combined water fills only a minor role, if any, in the bloating of the clays, slates and shales. The composition of the raw materials and especially the quantity of such gas-forming minerals as carbon, sulfur and their compounds doubtless control the type and extent of bloating. Thus free carbon, carbonaceous substances, carbonates, sulfides, any oxysulfur mineral compounds, and conceivably any other compound that will liberate a gas directly or as a reaction product of two or more of the constituents, are all potential bloating agents. The other basic requirement is that a softening or incipient fusion of the material occurs under the influence of heating coincident with the liberation of the gas. A softening of the mass in a highly viscous state facilitates the bloating by entrapping the gas bubbles. A uniformly slow liberation of gases evenly distributed throughout the expanding mass produces a superior product and assures better control.
Since the major demand for lightweight concrete block is in high construction areas, it is natural that facilities to produce lightweight aggregates would be located in or near the densely populated metropolitan centers. This segregation of production has set up well-defined market areas in which two or more lightweight aggregates are generally available and competing with one another.
The demand for lightweight aggregate for concrete masonry units derives, in part, from a desire to reduce the weight of masonry units and concrete block structures. The modular 8 x 8 x 16 in. hollow loadbearing air-dry concrete block in the current two-and three-cell designs, composed of ordinary aggregates, such as sand and gravel or crushed stone, weighs approximately 45 lb. Its counterpart of lightweight aggregate averages about 30 lbs and may weight as little as 221bs. Lightweight aggregates impart other properties desirable to concrete masonry units and masonry construction that are perhaps of even greater importance than their weight. These include increased thermal resistance, sound absorption, fire resistance, and nailability. Some lightweight aggregate types also contribute certain color shading and textural effects to concrete masonry construction that have been utilized for the interior treatment of auditoriums, school rooms, churches, office buildings, hospitals, and private dwellings.
The largest outlet for lightweight aggregates is in the manufacture of all types of precast building units in which nailability, ease of channeling, and heat-and sound-insulation are the properties desired. In the construction of large buildings, the lightweight of the finished concrete is essential, but in residential construction it is merely advantageous.
89
In general, the procedures for proportioning and mixing heavyweight and lightweight aggregate concretes in block manufacture are the same. There are some differences in detail, however, which arise from the differences in aggregate unit weight, particle characteristics, and water absorption. Most concrete products plants are equipped with traveling batchers operated in conjunction with overhead supply bins or silos for proportioning concrete materials. The batchers are either designed so they may be used for either weight proportioning or volume proportioning. Weight batching is probably in greater use. Some users of lightweight aggregates for concrete block prefer to proportion aggregate on a volumetric basis because of the lesser effect of moisture variations. Either method requires watchfulness of variations in moisture content as well as unit weight in delivered aggregate so that the established grading and yield and strength of block are maintained.
The most widely used mixer is the fixed-drum revolving-blade batch mixer. This type ranges to 80 cu. ft. in capacity and is evidently well adapted for preparing dry-mix lightweight aggregate concrete. There is rather general agreement in the industry, that lightweight aggregates need to be prewetted in the mixer before the cement is introduced. This practice is said to serve the dual purpose of satisfying the immediate absorptivity of the aggregate and of preventing cement from being drawn into large voids and interstices of rough-surfaced aggregate particles where it is presumed to be ineffective and to add useless weight. Tests conducted by the NCMA using 50 cu. ft. capacity mixers of conventional design, indicate that the mixing time, including the prewetting period of lightweight aggregates, should not be less than 5 minutes.
The use of air-entraining additives in producing lightweight aggregate concrete block is increasing. Entrained air is said to improve concrete moldability and cohesion of freshly molded units, particularly where aggregate particles are angular and rough-surfaced. It also improves concrete durability.
Probably the most important properties of lightweight aggregates are unit weight, grading, and strength. They determine to a considerable extent the weight of the product and the cement requirements to meet given strength stipulations. Other properties affecting final results include color, absorption, freedom from deleterious substances, particle shape, and particle surface characteristics. In general, savings in dead weight of 30 to 40 percent may result through the use of masonry units of lightweight aggregate. The lighter units also cut construction costs by providing greater ease of handling and higher output of mason labor. The increase in mason productivity, for example, has been estimated at 20 percent for lightweight over similar heavyweight units.
Lightweight aggregates also offer greater thermal volume stability than their heavyweight counterparts. This advantage is offset somewhat, however, by the generally higher drying shrinkage of the lightweights. Investigations at the University of Toledo's Research Foundation suggest that the higher drying shrinkage of walls composed of lightweight units is compensated in part by greater extensibility, since the modulus of elasticity of lightweight aggregate concrete for block ranges from one-half to two-thirds that of heavyweight
90
aggregate concrete. And, finally, published data on the sound absorption of masonry walls of commercial grade units indicate that those of lightweight aggregates have higher sound absorption efficiency than those of heavyweight aggregates, when left unpainted.
Various deleterious substances can and do occur in lightweight aggregates, and appropriate tests are described in ASTM specifications for their detection and limitation. Some of the better known contaminants peculiar to the different lightweight aggregates are: iron and iron compounds, hard-burned lime, clay lumps, and unburned or partially burned coal. Iron contamination is encountered principally in coal cinders. Iron and some of its compounds produce unsightly staining on exposed masonry surfaces and can also cause popping.
But as the recent spectacular growth in the use of lightweight aggregates for concrete block clearly indicates, the advantages of these natural and artificially produced lightweight materials greatly offset the disadvantages, at least in the calculations of the architects and builders who are using lightweight block in impressive numbers.
The future of concrete block is joined firmly to the growth and expansion and refinement of lightweight aggregates. A nation building skyward gives every indication of doing a large part of it with lightweight concrete block.
WEIGHT OF AGGREGATE AND CONCRETE BY TYPE OF AGGREGATE
TYPE OF AGGREGATE
AGGREGATE WEIGHT PER CUBIC FOOT POUNDS
WEIGHT PER CUBIC FOOT OF CONCRETE USING AGGREGATE POUNDS
POUNDS POUNDS
Gravel 120 150
Sand 90-100 150
Crushed Stone 100 145
Crushed Bank Slag 80 110-130
Haydite 40- 60 100-120
Foamed Slag 40- 60 90-100
Cinders 40- 50(+ Sand) 110-115
Pumice 30- 60 60- 90
Diatomite 28- 40 55- 70
Perlite 6- 16 40- 65
Vermiculite 6- 10 25- 50
91
WEIGHTS OF CONCRETE MASONRY WALLS CONSTRUCTED OF HEAVYWEIGHT AND LIGHTWEIGHT AGGREGATE MASONRY UNITS
Actual unit sizes (width x height x length), in.
Nominal wall thickness in.
Number of units Heavyweight aggregate, lb*
For 100 sq. ft. of wall Average weight of finished wall Weight savings
Lightweight aggregate, lb†
Mortar,‡ cu. ft. lb Percent
35/8 x 35/8 x 155/8 4 225 3050 2150 4.3 900 29.5
55/8 x 35/8 x 155/8 6 225 4550 3050 4.3 1500 33.0
75/8 x 35/8 x 155/8 8 225 5700 3700 4.3 2000 35.0
33/4 x 5 x 113/4 4 221 3000 2150 3.7 850 28.3
53/4 x 5 x 113/4 6 221 4500 3050 3.7 1450 32.3
73/4 x 5 x 113/4 8 221 5650 3700 3.7 1950 34,5
35/8 x 75/8 x 155/8 4 112.5 2850 2050 2.6 800 28.0
55/8 x 75/8 x 155/8 6 112.5 4350 2950 2.6 1400 32.3
75/8 x 75/8 x 155/8 8 112.5 5500 3600 2.6 1900 34.6
115/8 x 75/8 x 155/8 12 112.5 7950 4900 2.6 3050 38.4
Table based on 3/8-in mortar joints.
* Actual weight within + 7 percent of average weight.
† Actual weight within + 17 percent of average weight.
‡ With face-shell mortar bedding. Mortar quantities include 10 percent allowance for waste droppings within the core space and extrusion beyond the bearing areas of units.
92
Atmospheric or Low Pressure Curing of Concrete Block
By Benjamin Wilk
It is a far cry from the simple "sun kissed" or "sprinkling" curing of concrete block of the early 1900's to the sophisticated, controlled high-temperature and so-called "carbonation" curing of the late 1960's.
Producers found out early that concrete that dried out too fast was low in strength and wasteful of cement. Sprinkling with water for seven days was an early specification. Curing for 28 days before delivery was also an early specification.
In 1908, Rudolph J. Wig, assisted by Robert E. Ravlik, completed an investigation at the U.S. Geological Survey Laboratories in St. Louis to determine the effect of different steam pressures and the duration of steam exposure on the hardening of Portland cement mortar.
This was the first extensive scientific series of tests on steam curing of concrete products ever made, and the researchers discovered among other things that:
Steam up to 80 pounds per square inch gauge pressure had an accelerating action on hardening.
Compressive strength increased as steam pressure and/or time ofexposure were increased;
Compressive strength considerably in excess of that obtained after aging six months might be obtained in two days by curing with steam under pressure;
Concrete cured by high pressure steam was more uniform in appearance and lighter in color; Concrete should obtain an initial set before exposed to steam.
In spite of these positive conclusions, only a handful of plants adopted high pressure steam curing because the cost was prohibitive. Instead, early in the 1920's, researchers began to experiment with the idea of using
93 XI
steam at atmospheric pressures to obtain block that would reach a strength of 700 lbs per square inch in less than 28 days. The strongest block at that time were obtained with wet curing for 14 days, followed by 14 days in air at 70 degrees.
Coils of stream pipes on both sides of the curing kiln were used with small perforations in the pipe so that escaping steam would put moisture into the kiln. Temperatures up to 100 degrees and more were obtained which did hasten the hardening of the block materially.
In Detroit, a mechanical engineer named Morris H. Gross, who specialized in heating, became interested in studying how to improve the curing of concrete block. He worked with a miniature kiln to study the relationship between high temperatures, moisture, and strength, then came up with the idea that instead of introducing steam through pipes on the sides of the kiln, it would be simpler and better to put a single pipe at the front, near the top of the kiln, and project it into the kiln a short distance. Even with a low pressure boiler of 15 pounds, steam could be shot into a kiln of fifty or sixty feet at such velocity that the steam would hit the back wall of the kiln and cause enough turbulence to obtain uniform temperatures throughout the kiln.
Under the guidance of Mr. Gross, an extensive series of tests were made at the plant of the Wm. Moors Concrete Products Co. in Fraser, Michigan. The results of these tests were reported in Concrete Products Magazine in Feb. 1947 and August 1948.
To obtain information on the effect of high temperatures on the strength of block, five kilns were used with varying curing conditions. Kiln # 1 had steam that was cut off when a temperature of 199 degrees was reached. In kiln #2, steam was turned off at 170 degrees, while in Kiln #3, steam was cut off at 170 degrees by intermittently turning steam on and off for the entire curing period. Kiln #4 was the same as Kiln #3 except that a temperature of 140 degrees was maintained. Kiln #5 had steam on until 140 degrees was reached, when it was turned off.
Figure 58 shows comparative strengths of block for various methods of steam application. It is apparent that the method used in Kiln #2 is far superior to the other methods.
Temperature observations within the block and the kiln air were obtained with six thermocouples. A quick change switch made it possible for all six readings to be taken within 60 seconds. Thermocouples were placed in the kiln as follows:
In the shell of a block in the top pallet;
94
In the shell of a block on the fourth pallet;
In the shell of a block on the sixth or bottom pallet;
Kiln air at ceiling;
Kiln air midway between ceiling and the floor;
Kiln air at the floor.
An assembly was also arranged whereby a pallet of three blocks could be weighed during the curing cycle coincident with the temperature readings. This was provided by placing a platform scale, accurate to 0.01 lb, on the roof of the kiln with a chain connected to an attachment on the scale platform. The chain was inserted through a small hole in the roof of the kiln, with the bottom end of the chain fastened to a hanger that held the pallet with the three block suspended midway between the ceiling and the floor. The results observed for the intermittent readings of the six thermocouple temperatures and scale weight are shown in Fig. 59.
The steam was turned on at 10 a.m. and turned off an hour and 20 minutes later, when the temperatures of the air in the kiln and the temperatures within the concrete block shells approached equalization. This length of time for steaming was established from the theory that the concrete masonry units would take on moisture when they are cooler than the dew-point temperature of the surrounding kiln air, and they would lose moisture at equal temperatures due to the vapor pressure. The assembly suspended weight bore out this theory, since the weight increase diminished as the temperatures reached stability. This point of equal temperatures was called the point of equilibrium.
The steaming cycle is only one phase of curing under this method because the soaking period is also a definite factor for hydration of the cement products. As the temperature in the kiln decreased, the relative humidity increased because the moisture in the kiln remained relatively constant. Therefore, as long as the air temperature within the kiln was above 70 degrees, the condition within the kiln was favorable for accelerated curing in a highly humid atmosphere and the moisture necessary for hydration was not removed from the masonry units. When the temperature within the kiln was brought beyond the point of equilibrium, then moisture was removed from the concrete, which placed the concrete units in a condition unfavorable for hydration even though the atmosphere was of a high humidity because this moisture so essential for hydration was not replenished during the soaking period.
95
The temperatures are graphically described for the concrete block (thermocouple No. 2) and the kiln air (thermocouple No. 5) in Fig. 60. This figure shows the curing conditions during the presetting, steaming and soaking periods.
No definite conclusions were established from the specimens of kilns No. 3 and No. 4 wherein strengths developed were far below strengths of the specimens from the companion kilns No. 2 and No. 5. The former had temperatures brought up to and held at 170 degrees F. and 140 degrees F., respectively, whereas the latter were brought up to the same temperatures followed by soaking periods. The time of exposure of the blocks within the kilns was practically 15 hr. for all the kilns from the time the doors were closed until finally opened. It was observed, however, that the specimens from kilns No. 3 and No. 4 at the time of sampling were completely saturated with water.
On the basis of these and other tests, it was determined that a 170 degree F. temperature maximum was best suited for the facilities at William Moors Concrete Products Co., when running concrete block and 180 degree F. for cinder block.
Summing up, Mr. Mansfield said: "It would seem, then, that the amount of water contained in the unit would be the factor controlling shrinkage rather than the per cent moisture content. In fact, a specification limiting moisture to 4.5 lbs per cubic foot, which is equivalent to 30 per cent moisture content as per specifications, would be more practical, and if such a requirement were incorporated the above specimens would meet the specifications for two exceptions, the very ones that are more favorable under present specifications."
It is interesting to see how close the results at the Wm. Moors plant compare with a study made by the National Concrete Masonry Association in cooperation with the F. Hurlbut Company, Green Bay, Wis consin; Cleveland Builders Supply Company, Cleveland, Ohio; and the Plasticrete Corporation, Hamden, Connecticut-in July, 1947.
The study was under the direction of the NCMA's subcommittee I on Curing Methods, Technical Problems Committee, consisting of Paul M. Woodworth (chairman), Philip Paolella, Glenn C. Barnes, Benjamin Wilk, and Herb A. Davis. Jay Ehle, chairman, Technical Problems Committee and R. E. Copeland, NCMA, served as ex officio members.
The principal purpose of the investigation was to provide reliable data on the effect of variations in curing temperatures and cycles on the compressive strength of block. The effect of these variables on other properties of the block, together with auxiliary data pertinent to curing methods, were also obtained. Study of the data (See Fig. 61) suggested the following conclusions:
96
There is no critical curing temperature giving best results. In general, somewhat higher results were obtained with maximum temperatures in the 160 to 180° F. range than at higher or lower temperatures;
Compressive strengths at three days age or greater were not decidedly inferior with curing at 130° F. than at higher temperatures;
Reducing the holding period to less than 2 hours or prolonging the steam-on period beyond 13 hours appeared to decrease strengths of sand-and-gravel block;
Compared with 13 hour continuous steaming, equally good results were obtained with a 4 hour steamon period followed by 9 hour soaking (In this connection it should be noted, that during the soaking period kiln temperatures decreased from about 3 to 5° F. per hour from a 200° F. maximum, about 2 to 4° F. per hour, from a 170° F. maximum and less than 1° F. maximum per hour from a 130° F. maximum.);
Celocrete groups #14 and 15, steam cured for only 4 hours were noticeably inferior, especially at early ages, to units cured for longer periods.
Considering the most favorable cycles, the 28 day strengths were in excess of 85% of the strengths obtained with prolonged (14 days) moist curing. Had these specimens been allowed to dry less rapidly (as would be the case with storage in stockpiles), it is believed this percentage would have exceeded 90% and probably averaged at least 95% of the moist cured strengths. It appears therefore, that live steam curing when properly applied, is highly effective.
For those manufacturers employing high temperature curing the following cycle was recommended by the NCMA subcommittee:
Maximum temperature: 165-175° F.
Holding period: approximately 2 hours;
Steam-on period: time required to attain maximum temperature, plus 1 hour, with the total steam-on period to be not less than 3 hours;
The rate of temperature rise in the kiln should not exceed about 60° F. per hour;
Soaking period: 8 hours minimum and longer if practicable.
97
Regarding proper steam boiler pressures, evidence indicated that low pressure steam (10-15 lb. per sq. in.) should be employed in curing block made with dense aggregate. Block made with lightweight aggregate apparently have a greater tolerance to and can be effectively cured with considerably higher steam boiler pressures.
Several years later the NCMA instituted a six-year study of the effects of siliceous materials in the curing of concrete block at atmospheric temperatures. The study was described (See Fig. 62) by Henry Toennies, NCMA Director of Engineering, and Thomas B. Redmond, NCMA Autoclave Engineer, in the NCMA booklet "Siliceous Fines in the Cementing Medium of Steam Cured Concrete Masonry Units." Some of the principal conclusions of the study included:
The compressive strength of block containing portland cement only was generally higher than block with siliceous material replacement at most kiln-curing temperatures (See Fig. 63 ); At high kiln-curing temperatures, a number of mixes containing either ground pumice or fly ash yielded strengths as great or greater than those of reference mixes;
The strength of some aggregate type units was more affected by different curing temperatures than others. Expanded shale mixes consistently showed the greatest variation in strength with temperature change, while limestone and expanded slag mixes showed the least (See Fig. 64) ;
The performance of siliceous materials in order of their relative merit was fly ash, ground pumice, and silica flour;
Use of a constant temperature cycle in lieu of soaking generally improved the compressive strength of mixes cured below 185 degrees F., but resulted in the same or lower strengths for higher curing temperatures;
When fly ash or ground pumice is used as a partial replacement for portland cement, a kiln-curing temperature of 185 degrees F., or greater is usually beneficial.
Possibly because of the similarity of earlier test results, there was a lag of more than 20 years before another comprehensive study was made of steam curing. The American Concrete Institute finally took it on, publishing its results in 1969 under the title, Recommended Practice for Atmospheric Steam Curing. Perhaps not surprisingly, the recommendations are almost the same as those made 20 years ago (See Table 65).
In summarizing its study, the ACI says: "The recommended steam curing cycle for concrete masonry units depends to some extent on the composition of cementitious materials and aggregate type. For normal weight aggregate block, the presteaming period should be a minimum of 2 hours at 60 to 100° F. during warm weather and one hour longer
98
in cold weather. The temperature rise should not exceed 60° F. per hour to a maximum of 150 to 165° F. After reaching maximum temperature, the units should "soak" for a minimum of 12 hours, or until the required strengths are developed.
For lightweight block, a similar cycle is used, but the presteaming period may be reduced one hour and the maximum temperature may be raised to 180 to 190° F. When Pozzolans are used as part of the cementing medium, maximum temperatures of 200 to 210° F. should be investigated for both lightweight and normal weight aggregate units. Controlled plant tests are recommended to refine the times and temperatures desired to produce optimum results in individual plants. The use of consulting engineering services for design of curing facilities is highly recommended.
In the past year, there have been a number of installations of new low pressure steam curing systems in plants throughout the United States, many including some form of drying sometimes coupled with carbonation. The recommended practice deals generally with these subjects as follows: "At completion of the steaming cycle, concrete masonry units are wet and many require drying in order to comply with ASTM C90. Air drying is most often used for reducing the moisture content of masonry units. Air drying permits some additional hydration and strength gain after the steaming cycle, but requires a larger inventory of product and requires covered storage in most climatic areas. Artificial drying may be accomplished in the steam curing kiln while the masonry units are still on the curing rack, or it may be performed in a separate drying room after the units have been removed from the rack and stacked in the cubes. The objective of artificial drying is a rapid lowering of the moisture content in the masonry unit. Another possible advantage in producing hightemperature air for artificial drying by means of direct firing or combustion gases is the carbon dioxide produced which may effect carbonation of the masonry units." (The exact effects of carbonation are still uncertain, but are generally considered beneficial.)
In a paper presented at the 1969 NCMA National Convention, C. E. Lovewell, Vice-President for sales and engineering of the Chicago Fly Ash Co., had this to say about the ACI recommendations:
“Because the Recommended Practice lacks enough specific information to provide a valid basis for the average block producer to decide whether or not to add a drying cycle or drying plus carbonation I made an additional search for information through experimentation and the reading of available literature. It became quickly apparent that effective carbonation of steam cured masonry units causes irreversible shrinkage and, if accomplished prior to use in construction, amounts to preshrinkage. Combination drying and carbonation systems, following saturated steam curing, are on the market and are being installed by block producers in increasing numbers.”
99
"Technologists have proven that carbon dioxide, coupled with heat and a drying atmosphere, combines with the hydration products of cement to form carbonates. Lime, one of the principal hydration products, goes from calcium hydroxide (a relatively weak compound of large volume) to calcium carbonate (a relatively strong compound of smaller size). Quoting from the Concrete Industries Yearbook, 1968 Edition: The improvement of surface structure of concrete block by the absorption of carbon dioxide (CO2,) has long been known. Products such as cast stone and sand lime brick are vastly improved by carbonation. The effects of such treatment on the hardened products of portland cement concrete include: the increase of tensile and compressive strengths; the increase in the modulus of elasticity and hardness; the increase in density to some degree; the production of considerable shrinkage while the carbonation is taking place; and the reduction of moisture volume change (shrinkage from wet to dry condition) by about 50%.”
"Research has shown that it takes about one pound of CO2, (carbon dioxide) to fully carbonate an 8 x 8 16" concrete masonry unit if made with portland cement as the only cementing material. Other research has shown that effective, although not complete, carbonation can be secured by blowing hot combustion gases from a gas burner into the curing kiln as the final phase of the curing cycle. Both drying and partial carbonation are accomplished to greater or lesser degree, depending upon a number of considerations including:
Proper baffling or ducts to make sure combustion gases are equally distributed throughout kiln;
Temperature and concentration of CO2, in gases;
Duration of treatment, presumably at least long enough to bring blocks to specified dryness;
Whether fly ash or other pozzolan is used as partial (say 20 to 35 per cent) replacement for cement, thus reducing by like per cent the amount of cement hydration products to be carbonated.”
"Thus, there is a greater awareness in the block industry that by optimum use of available quality ingredients approved for use in manufacture of concrete masonry units in ASTM C90, and that by installing equipment of proper capacity and design, operated in the optimum cycle, it is possible to produce, economically, low pressure steam cured concrete masonry units meeting the most rigid specifications for dryness and shrinkage currently being written. It is highly recommended that before investing in such facilities, block producers carefully scrutinize the various drying and carbonation systems being offered commercially and check with fellow producers outside their own marketing areas as to the successful performance being achieved with each."
100
Fig. #58
COMPARATIVE STUDY OF STEAM APPLICATION METHODS
Kiln Number 1 2 3 4 5
Degrees 199 170 170 140 140 Door Closed
11:10 a.m. 9:16 a.m. 11 :30 a.m. 2.00 p.m. 8:46 a.m. Steam On 2:00 p.m. 11.35 a.m. 2:30 p.m. 4:00 p.m. 11 :00 a.m. Steam Off 2:30 p.m. 1:00 p.m. 2:30 a.m. 8:00 a.m. 11 :36 a.m. COMPRESSIVE STRENGTH
28 hours 1 1 866 1420 692 413 916 1 4 821 1279 573 463 849 1 6 861 1285 531 390 560 Average 789 1328 599 422 775 7 days 1 1 1015 1695 1033 741 1366 1 4 1162 1559 768 629 1248 1 6 1149 1938 797 803 1309 Average 1109 1731 866 724 1308
28 days 1 1 1714 1191 821 1465 1 4 1700 1100 966 1454 1 6 1911 989 1024 1420 Average 1775 1093 937 1446
*The 28-day specimens for Kiln No. 1 were lost by inadvertently being placed in yard storage.
Fig. #59
KILN CONDITIONS DURING CURING CYCLE
Thermocouple Temperature
Suspended Weight
Time 1 2 3 4 5 6 Assembly Net Change Per Block
8:15 a.m. 72 68 69 97 82 79 187.62 10:00 97 79 77 99 87 81 187.60 -0.04
10:16 114 109 114 126 123 122 188.69 +0.32
10:30 130 128 134 137 134 135 189.34 +0.57
10:46 142 142 144 149 147 147 189.76 +0.71
11:00 166 164 156 159 157 157 190.38 +0.92
11:15 164 164 165 168 167 167 190.87 +1.08 11:20 170 170 169 171 170 170 191.01 +1.13 11:21 167 166 169 168 165 162 191.01 +1.18 11:26 168 166 166 164 163 16E 191.01 +1.08 11:30 168 166 151 164 162 147 190.86 +1.04
12:00 163 162 136 161 157 132 190.76 +1.04 12:30 a.m. 159 156 132 157 154 125 190.76 +1.04
1:00 155 153 127 154 150 122 190.76 +1.04
1:30 166 150 127 152 148 119 190.75 +1.04
2:00 154 147 127 153 147 119 190.76 +1.04 2:30 152 144 126 150 144 119 190.76 +1.04
8:00 149 142 124 148 143 118 190.75 +1.04
4:30 146 134 118 143 140 118 190.76 +1.04
101
Graph shoving curing conditions during the presetting, steaming end socking periods
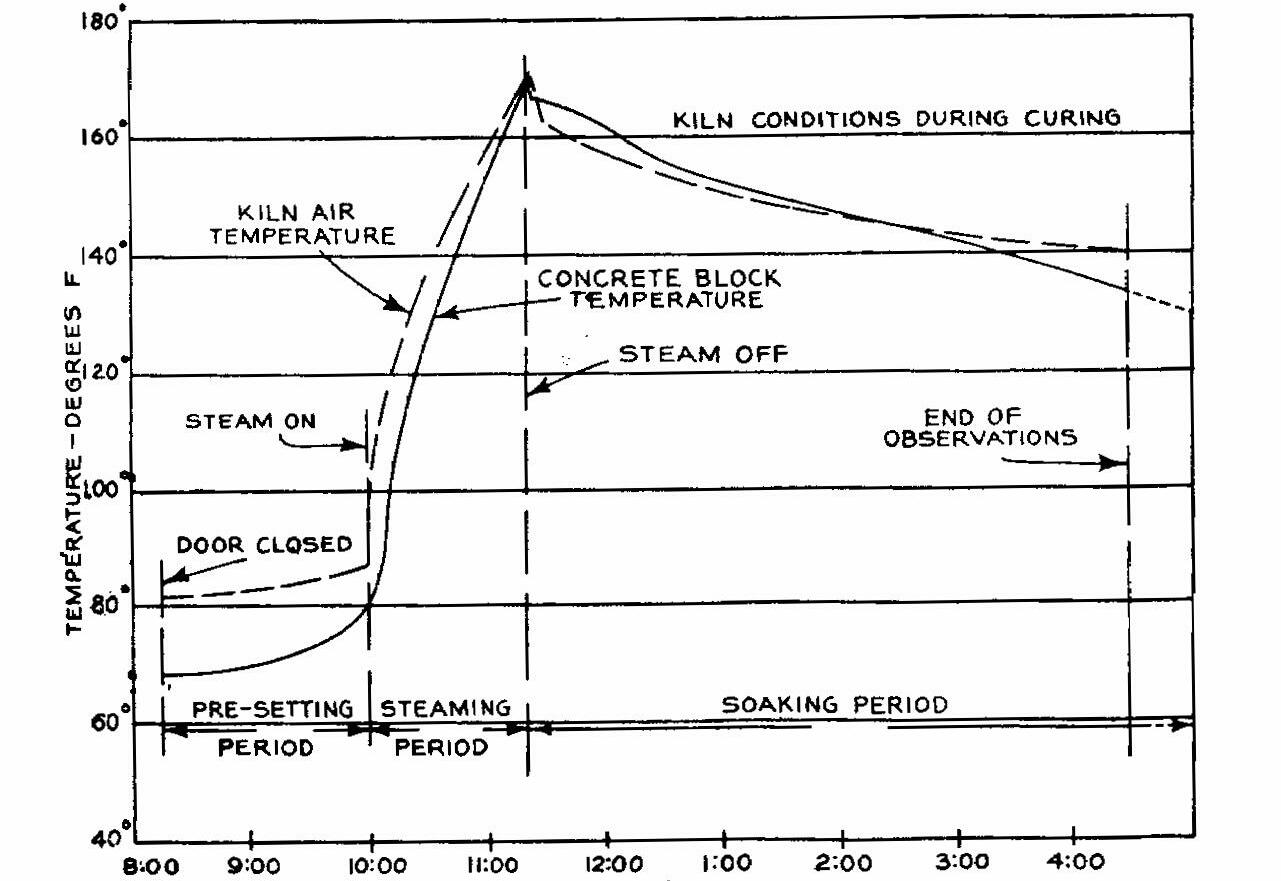
102 Fig.#60
Fig. #61
SUMMARY OF RESULTS OF TESTS OF EFFECT OF VARIATIONS IN CURINGTEMPERATURES AND CYCLES ON COMPRESSIVE STRENGTH OF BLOCK SPECIMENS AT 3, 7,AND 28 DAYS AGE *
Curing Cycle Periods, Hr.
Strength Ratio ControlSpecimens Specimens Cured Steam ; % ‡
Group Ref. No. Max. Temp. OF Holding Steamon Soaking Hot Air Drying Total 3-Days 7-Days 28-Days
Sand and Gravel Block Specimens (Specimens made at F. Hurlbut Co. Plant)
1-3 1-10 2 3
180 180 180 180
2 2 2 1
13 13 19 13
1 1 1 1
3 10 3 3
19 26 25 18
74 76 73 64
180 180 180
2 2 2
4 8 8
4 1 5
3 3 3
13 14 18
66 66 71
Celocrete BlockSpecimens (Specimens made at Cleveland Builders Supply Co. Plant)
83 87 78
81 .... 83
84 86 82
91 85 71 66 4 5 160 140 2 2 13 13 1 1 3 3 19 19 69 79 84 84 83 6 7 8
1 2 3 4
200 200 200 200
2 2 2 2
13 8 4 4
0 9 5 5
0 0 0 0
15 15 15 11
75 75 76 65
80 83 77 77
84 84 84 78 5 6 7 8
170 170 170 170
2 2 2 2
13 8 4 4
0 9 5 5
0 0 0 0
15 15 15 11
77 74 75 75
85 82 83 81
86 86 94 91 9 10 11 12
130 130 130 130
2 2 2 2
13 8 4 4
0 5 9 5
0 0 0 0
15 15 15 11
73 59 67 64
77 74 80 72
83 81 85 85 14 15 200 200 2 2 4 4 0 0 0 0 6 6 54 63 67 66 75 76 (Group 15 mix contained 1 lb. cal. chloride per sack of cement.) Cinder BlockSpecimens (Specimens made at Plasticrete Corp. Plant)
1 2 4
200 200 200
2 2 2
13 8 4
0 5 5
0 0 0
15 15 11
84 79 81
98 99 104
104 102 102 5 6 8
170 170 170
2 2 2
13 8 4
0 5 5
0 0 0
15 15 11
96 91 88
97 99 104
115 115 101 9 10 130 130 2 2 13 8 0 5 0 0 15 15 85 90 102 95 99 112
* Tests conducted by National Concrete Masonry Association with cooperation of member plants indicated.
‡ Compressive strength of control specimens at 28 days = 100%. Control specimens were moist cured at 65 - 75º F. for 14 days then stored in laboratory air for 14 days.
103
Series
1A
1B
2A
Concrete Mix
Curing Cycle
2B
Purpose of Series Aggregates* Cementitious Materials Hour Temp F
To determine the optimum replacements of portland cement with siliceous materials and lime for autoclavecured block
To compare a 24-hour single-stage cure of Series 1A
To determine effective maximum temperature for kilncured block containing siliceous materials
To compare effect of holding maximum kiln temperature constant to the soaking procedure of Series 2A
Sand-Gravel Limestone Exp.Slag Exp. Shale Cinders Pumice Scoria
Cement (1)
Fly Ash Silica Ground Pumice Exp. Shale Fines Lime†
Preset Period
Heating Rate Deg/Hr
Max Temp F
Time At Max Temp Hr
Soaking Period Hr
2 7480 100 362 5 0
Physical Test
Exp. Slag Exp. Shale
Sand-Gravel Limestone Exp. Slag Exp. Shale Cinders
Cement (1) Fly Ash Silica 2 7480
(Kiln) 4550 (Autoclave) 100
180 362
Cement (1) Fly Ash Silica Ground Pumice
(Dense) 2 (LW) 1
7480
(Dense) 40 (LW) 50
0 5 & 20 0
Compressive Strength Absorption Drying Shrinkage Rupture Modulus‡
Compressive Strength Absorption Drying Shrinkage Rupture Modulus
Varies 140240 0 12 Compressive Strength Absorption
Sand-Gravel Limestone Exp. Slag Exp. Shale Cinders
Cement (1) Fly Ash Silica Ground Pumice
(Dense) 2 (LW) 1
7480
(Dense) 40 (LW) 50
Varies 140240 12 0 Compressive Strength Absorption
* Filler aggregate material used with expanded slag and cinders for Series 2A and 2B
† Use of lime limited to sand and gravel, expanded shale, and expanded slag batches.
‡ Rupture modulus determinations made on expanded slag and expanded shale units only.
104
Fig. #62
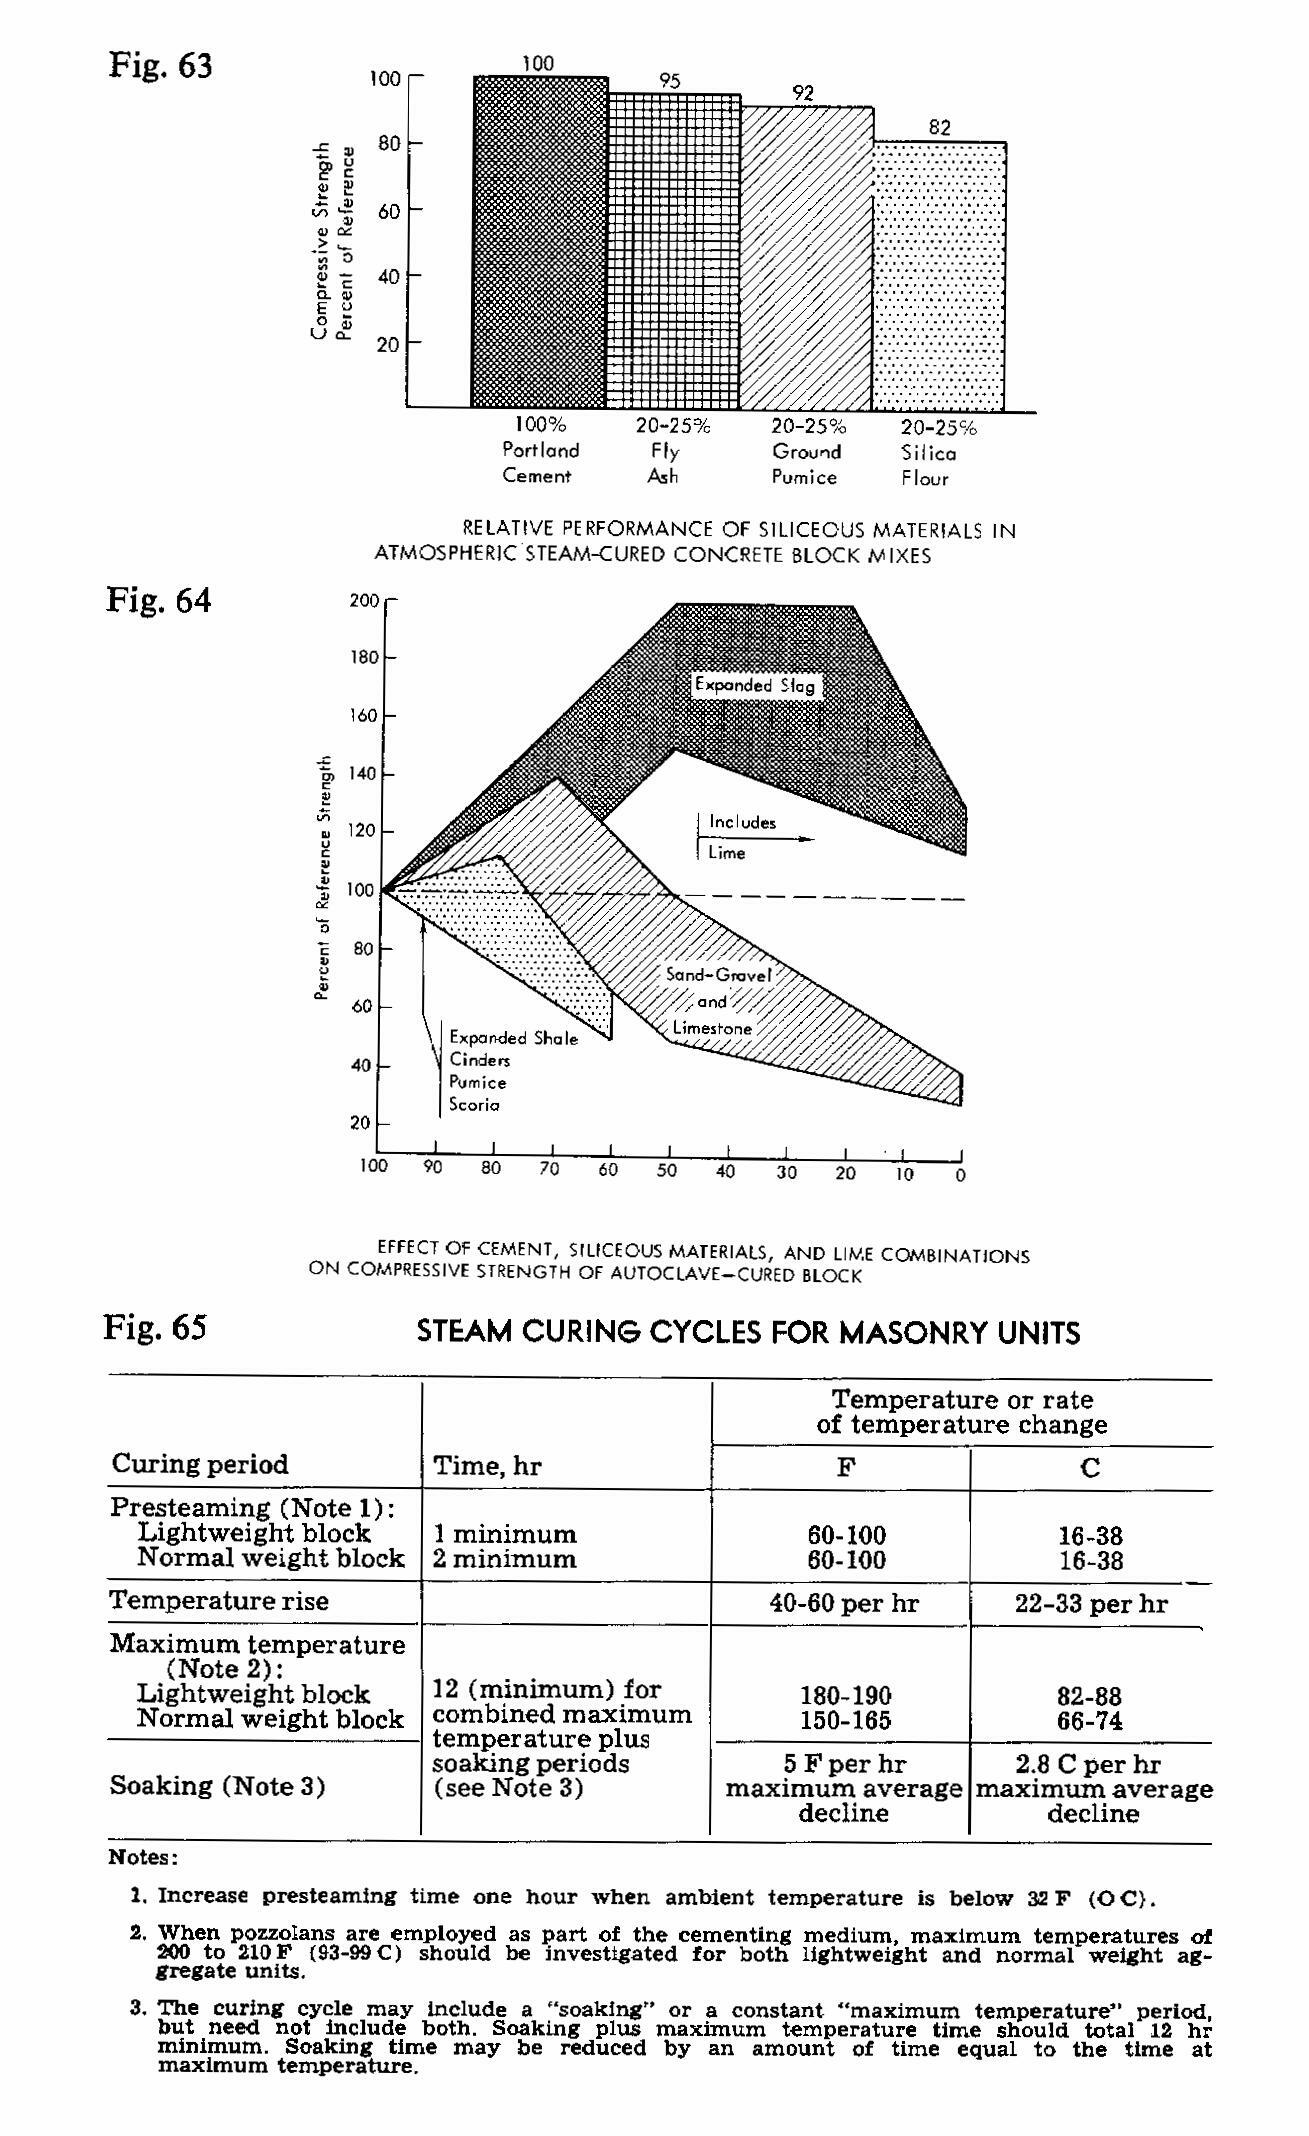
105
Autoclave Curing
By Carl Menzel
For 40 years the primary purpose of curing concrete block in saturated high pressure steam in autoclave cylinders was to produce high quality block in the shortest time at the lowest cost. Various individuals, researchers, associations, technical committees, block producers, autoclave plant equipment manufacturers, and design engineers worked toward this objective and are continuing to make improvements. As a result high quality, reasonably volume stable and dry autoclaved block can now be ready for use within 12 hours after molding, and autoclave curing has become one of the major developments of the concrete block industry.
Great credit for this achievement is due the relatively few pioneers who blazed the trail from the 1930's to the early 1950's for the commercial use of autoclave curing. They had faith and persistence, against great odds, in their belief that autoclave curing of concrete block was practical.
The Crume Brick Co. of Dayton, Ohio was such a pioneer. It began making sand-lime brick about 1909 and cured them in autoclaves to harden the brick by the lime-silica reaction which occurs in saturated steam at high temperatures and pressures. However, by 1929 this brick producer was concerned about the increasing competition of concrete block and its advantage of size of unit. He also observed that the many advances being made in the concrete block industry were not being matched in the sand-lime brick industry.
Chief among these advances were better block machines, mixers, and procedures. There were also the favorable results of an extensive series of fire tests on concrete masonry walls at Underwriters' Laboratories, sponsored by the National Concrete Masonry Association, the Portland Cement Association and by such individual producers as F. J. Straub (of cinder block fame) and the Western Brick Co., producer of lightweight expanded shale (Haydite block). Finally, there was the promotion of block by the NCMA and PCA.
As a result, the Crume Brick Co. started to produce wetcast 5 x 3/4 x 12 in. two-core concrete tile units made with sand and gravel and portland cement as the primary binder. Crume found it could make an excellent product by curing the units in their molds on cars in the same autoclaves already available for making sandlime brick.
The Crume Brick Company's efforts came to the attention of the Portland Cement Association in Chicago, where W. D. M. Allen and Paul M. Woodworth began studying the process and the properties of the
106 XII
concrete tile made by the Crume plant. Their studies showed that the two-day compressive strength of the auoclaved tile was about 55 per cent higher than the 28-day strength of tile moist cured at normal temperatures and more than twice the two-day strength of the cured in steam at atmospheric pressure. Of even greater importance, the tests indicated that autoclave curing reduced the drying shrinkage of concrete masonry panels laid up with wet units to less than half that of units cured in steam at atmospheric pressure. Moreover, when the masonry panels were laid up with air-dry, autoclaved units, the shrinkage was practically nil.
With this new favorable information, the Crume Brick Co. began autoclaving all its concrete tile units in 1930. This decision was strengthened by further studies showing that after one year the autoclaved units had strengths averaging about five per cent higher than those of similar units continuously cured moist for one year at normal temperatures. These comparisons were based on units tested in a damp condition. By 1939, the entire plant capacity of the Crume Brick Co. was devoted to the manufacture of concrete brick and 8 x 8 x 16 in. concrete block with additional autoclaves to handle the output of high production machines.
Allan and Woodworth reported the favorable results with the autoclaved Crume concrete tile in three American Concrete Institute papers in 1930 and 1931. An extensive series of tests with high pressure steam curing were then made in the research laboratory of the Portland Cement Association (under the direction of C.A. Menzel) to answer many questions that might lead to widening the scope of autoclave curing of concrete. The results of these tests were reported in ACI papers in 1934, 1935 and 1936.
Besides confirming the favorable results reported by Woodworth and Allan; the new series of tests brought out the important effects of silica and various finely divided silica-bearing materials on the strength and drying shrinkage of autoclaved mortar and concrete. Moreover, they indicated that in the absence of siliceous fines in the aggregate, a replacement of as much as 40 per cent of the portland cement by pure silica as fine as the cement could be accomplished with good results. The tests also confirmed the improvement in resistance to the action of sodium and magnesium sulphate solutions obtained by autoclaving cement mortar and concrete, and indicated that the strength and stability of autoclaved block was permanent.
In view of the published technical information of the improvements that could be obtained by curing concrete in high-pressure saturated steam, it is not surprising that during the period 1930 - 1940 sand-lime brick plants all over the nation started to divert part or all of their production to the manufacture of 8 x 8 x 16 in. concrete block, using the same autoclaves already available for making sand-lime brick. In spite of the depression years, autoclaved block found a ready market.
Among the pioneers who began autoclaving concrete block in the 1930's were Luther G. Randolph, Harold J. Levine, J. Morely Zander and Winter Ferguson. These enthusiastic men, dedicated to improving the quality of
107
concrete block, shared their information on costs, plant design and operation with other block producers who were contemplating conversion to autoclave curing. In 1941, they joined such eminent researchers as Douglas E. Parsons, J. C. Pearson, Paul M. Woodworth and J. C. Chenery on a newly-formed ACI Committee on "High Pressure Steam Curing." This committee published a timely progress report in April, 1944 listing eleven conclusions based on available research and practical experience on the autoclaving process.
Armed with this positive, reliable information at the end of World War II, several block producers including Terry Carpenter, LTD., Scottsbluff, Neb.; Arkhola Sand and Gravel Co., Fort Smith, Arkansas; Harter Marblecrete Stone Co., Oklahoma City; Concrete Pipe and Products Co., Richmond, Virginia, among others turned to autoclaving with large new autoclaves and equipment. The many innovations at the Harter plant, with five large autoclaves 8' in diameter and 96' - 6" long, challenged the ingenuity of block producers all over the United States and Canada. Moreover, Noel Harter and his brother, B. D. Harter, were most generous in providing information and permitting inspection of their plant facilities. As a result eleven new autoclave plants started operation by 1956, and each in turn helped others.
The experience of each new autoclaver was so favorable that the number grew steadily in spite of the high initial investment. There were about 30 plants in the U.S. and Canada autoclaving block in 1955, 46 in 1956, 65 in 1957, 80 in 1958, 94 in 1959 and 112 in 1960 (thirteen of them in Canada.)
By 1965, the number of plants autoclaving block totaled 176, and two years later, the total had grown to 205 (with 35 in Canada.) Between 1960 and 1967, there was an increase of 93 plants an average of about 13 plants per year.
The 200 plus plants currently autoclaving block in the United States and Canada account for at least 20 per cent of all block produced. Both autoclavers and their customers especially architects and engineers have apparently been well pleased with the performance of autoclaved block. As a result many plants have been adding more autoclaves to meet the demand of satisfied customers, and some larger producers are now operating several new autoclave plants.
The advantages of autoclaving are not, however, confined to large plants. For example, Karl E. Kelly, Jewel Concrete Products, Inc., Waco, Texas, points out "We would like to say that a small manufacturer can afford to autoclave block in fact he cannot afford not to if he wishes to have a product that will continue to grow in acceptance by the architect." His plant produces 7,400 block per day, curing 3,700 units during each 12-hour shift in one autoclave 8' in diameter and 122' - 6" long by single-stage curing with contour racks.
During these years of progress and development in autoclaving, the organizations formed by block producers to serve their promotional and technical needs were turning an increasing amount of attention toward this process.
108
This was most evident in the Sand-Lime Brick Association. This group, devoted to sand-lime brick since 1906, changed its name in 1941 to the Autoclave Building Products Association because so many of its members started producing autoclaved concrete block in the 1930's. Two divisions were established, one for sand-lime brick producers and the other for concrete block producers. In this way autoclave block producers filled a need to promote their special interests especially through research and conventions where they could discuss mutual problems.
Interest in the Block Division of the ABPA increased during the 1940's under the leadership of such officers and members as Elmer R. Coats, Leo J. Ryan, Ralph E. Cromis, Henry DeGeus II, John Wheeler and Dale Cobb. By 1951, the annual conventions of ABPA were well attended by new producers of autoclaved block and those interested in converting to autoclaving, and during the following decade, attendance and interest grew steadily. During this period, John Selden became Technical Director and Coordinator of programs and prepared a monthly news bulletin called the Autograph
Meanwhile in the late 1940's and early 50's the bulk of the industry continued to cure block in saturated steam at atmospheric pressure at about 165 deg. F. The NCMA provided strong assistance to its membership in developing and using this method of curing to best advantage.
However, when it became apparent that interest in autoclave curing was increasing and that several large plants had converted from curing in steam at atmospheric pressure to high pressure steam at 120 to 150 psi., the NCMA established a Subcommittee (made up of six autoclaved block producers) devoted to High Pressure Curing. The committee outlined a technical and research program to be financed by contributions of regular NCMA members interested in autoclaving.
As one of its first steps, the NCMA commissioned Harrison F. Gonnerman, to prepare an "Annotated Bibliography on High Pressure Steam Curing of Concrete and Related Subjects." This monumental compilation, comprising 300 pages and covering the period 1868 - 1954, was published in 1954. The following year, NCMA published a 143page report on "Layout, Design and Installation of High Pressure Steam Systems for Curing Concrete Masonry Units," prepared by St. John, Platt and Carlson, Consulting Engineers, Buffalo, N.Y. Ronald E. Copeland and Henry Toennies of the NCMA staff also made significant contributions in their studies of the corrosion problem.
In 1958, NCMA sponsored a "Technical Conference on High Pressure Steam Curing" in Chicago following its 38th annual convention. The program included 30 speakers and panel discussion leaders with Clyde Stewart, as Conference Chairman. The proceedings of this important conference filled 94 pages and covered such timely subjects as: corrosion of racks and autoclaves; silica dust a health hazard; curing cycles and mix composition and proportions; single-stage and two-stage curing methods; autoclave loading and unloading; doors, gaskets and
109
general maintenance; autoclave size, layout and details; boilers and piping; properties of autoclaved units; need for crackcontrol measures; and reducing installation and operating costs.
Obviously autoclave block producers benefited by the activities of both the APBA and the NCMA, but much of their efforts were duplicated and in 1960 it became clear that still greater benefits could be achieved by a union of the two organizations. Consolidation committees were headed by Max H. Miller and Walter W. Underwood for the NCMA and John S. Wheeler and Clyde Steward for the APBA. The union was formally accomplished on January 28, 1961, when ABPA gave up its separate identity and became a new division of the NCMA, with equitable representation of former ABPA members on the NCMA Board of Directors and on the 12-man Autoclave Committee. As a part of the agreement, Thomas B. Redmond joined the NCMA staff as Autoclave Engineer assigned specifically to the interests of autoclave members and responsible for research and development of autoclave curing.
This merger generally considered a necessity for the future well-being of the concrete block industry has worked out exceedingly well. Numerous, timely, Autoclave Bulletins on a variety of subjects have been prepared by the Autoclave Division Committee for the information of NCMA affiliates. Some are of particular interest to producers of sand-lime brick and other autoclaved calcium silicate and cellular products or cement-asbestos products. Currently, a 25-member Autoclave Division Committee is working with four Task Groups in the specific interest of autoclave block producers, and there is also a strong liaison with the Main Technical Committee of the NCMA.
A landmark in this cooperation took place in November, 1968 when the NCMA conducted its first short course on autoclaving, for three days at Alexandria, Virginia. The course was well attended; among 78 enrollees were owners, plant managers and foremen from cities as far distant as Seattle, Washington, and Liverpool, England. Students were provided with the "NCMA Autoclave Reference Manual" the most extensive manual on autoclaving yet compiled. This new short course on autoclaving will augment the School for Block Making which has become a regular part of the NCMA service to members.
On April 2, 1969 the ACI and NCMA jointly sponsored an all-day Symposium on High Pressure Steam Curing, named in honor of Carl A. Menzel for his pioneering work on autoclaving. It comprised 12 papers some by Canadian and Russian authors discussing physical and chemical aspects of the autoclaving process, methods of evaluating raw materials, curing procedures, autoclaving of such related products as asbestos-cement and sandlime brick, use of pigments and trends in plant design. The papers were published in 1970 by the ACI in a symposium volume. This symposium demonstrated that significant advances in the technology and practical application of high pressure steam curing are still being made and that more can be expected as the various factors in the complex chemical reactions become better understood.
110
Among the pioneers in autoclave curing during the 1930's and 40's were several manufacturers of pressure vessels in the United States. The interest of their design engineers in producing safe and suitable autoclaves, doors, supports and other essential features was an important factor in helping block producers with their plans to convert to autoclave curing. Currently there are at least twenty-five such manufacturers interested in serving the block industry. Some have become specialists in developing and producing the autoclaves and accessories required for improvements in concrete block production.
From the very beginning the primary purpose of curing in high pressure steam was to improve the quality and uniformity of block. Hence, autoclave design and operation was guided by the known requirements for attaining high quality, stable block. Extensive research indicated that the special chemical reactions which occur during autoclaving of concrete block require a certain amount of time of exposure to saturated steam at favorable temperatures and pressures. Hence, a given autoclave curing cycle may be divided into four operating periods: preset, temperature rise, constant temperature and pressure, and finally, rapid pressure release.
The preset period never less than two hours must be long enough to develop sufficient hardness in the block to withstand handling into the autoclave and the subsequent exposure to steam. At least three hours should be allowed for the temperature-rise period, in order to bring autoclave temperatures and pressures to desired maximum values. The constant temperature and pressure period (until present research offers alternatives) should provide a full 5 hour exposure to saturated steam at a gauge pressure of 140 - 150 psi and 360 - 365 deg. F and a full 6 hour exposure to steam at 120 psi gauge pressure and 350 deg. F. And, finally, the rapid pressure release period commonly termed "blowdown" should reduce the steam pressure as quickly as possible (not more than 20 minutes) to atmospheric pressure.
Ingenious block producers and equipment manufacturers superimposed on these basic principles of autoclave operation a number of innovations in design and operating procedures that were practical and economical for given local conditions. Of special importance was the emergence of two general methods of autoclave curing: single-stage and two-stage. In the single-stage method, block are moved into the autoclave on racks without being removed from their steel pallets and are cured in one operation at normal temperatures after a preset time of at least two hours. In the two-stage method, block receive initial preset curing in ordinary steam kilns at atmospheric pressure and about 160 deg. F. until they are strong enough for removal from the racks and pallets for cubing or stacking on a train of cars. The train is then moved into the autoclave for final curing in highpressure steam.
Reliable data on the comparative cost per block of autoclaving by these two methods vary with plant conditions and locality, but each method has its ardent champions. It appears that if steam kilns for curing at atmospheric pressure are already available, the two-stage autoclaving method requires about 25 per cent less new capital expenditure for the high pressure curing phase than is required for the single-stage method. However, the final
111
cost of curing and drying will be less with single-stage, and at the present time, a substantial majority of the autoclave block plants in the U.S. and Canada are using the single-stage method.
Block producers are advised to hire a qualified engineer to study plant conditions and recommend the sizes and capacities of autoclaves and boilers to be installed. The diameter and length of autoclaves has been increasing during the past 25 years until units 10 ft. in diameter and 120 ft. long are common. (A few even exceed 150 ft. in length.) Costs per block per day usually decrease proportionately with the increase in diameter and length of the autoclave.
Steam from the high pressure boiler may enter the autoclave through a perforated pipe at one or both sides for distribution over the length of the autoclave and should not impinge on the block. Proper distribution is essential because the rapidly expanding steam under high pressure from the boiler becomes superheated and produces a drying action detrimental to the block until the steam again becomes saturated. This can be the source of considerable trouble, causing variations in both strength and color uniformity. Some producers introduce a water spray into the steam distribution pipes to reduce the superheating of the expanding steam during build-up.
During the past 10 years a number of "boilerless" autoclave installations have been made in which steam is generated by passing hot oil through coils covered by about 2 in. of water in the bottom of the autoclave. This provides a large surface for the distribution of saturated steam for the full length of the autoclave. Condensate is recovered in storage tanks under pressure for the next cycle, and rapid blowdown is accomplished without water in the autoclave. Since the heat source operates at atmospheric pressure, a fireman is not required in most areas. For this and other reasons, the number of "boilerless" autoclaves has been increasing.
Rugged, dependable leak-proof doors are, of course, essential to the proper operation of all autoclaves. There are two types in general use: bolted and quick-opening. Bolted doors, used for years in pressure vessels, are inherently safer than quick-opening doors, have a high gasket life and maintain a tight seal. But primarily because of the time element and resultant economies, most autoclaves in the block industry are now equipped with quick-opening doors which require about 2 or 3 minutes to open or close, as contrasted with about 20 minutes for bolted doors. Quickopening doors have been markedly improved during the past 15 years to make them safer, provide longer gasket life and reduce leakage of steam.
Racks are also an important adjunct to the autoclave curing of concrete block, and as with the doors there are two principal types: the straight rectangular rack that leaves considerable vacant space at the sides and top of the circular autoclave cylinder; and the contour rack, shaped to conform more nearly to the cylinder, thus increasing the block capacity of the autoclave as much as 40 per cent. Contour racks are used in the majority of plants using the single-stage curing method.
112
Racks are especially susceptible to corrosion, the chief technical problem of the autoclave block industry. Corrosion has been the cause of considerable maintenance and replacement expense in some plants, and special effort is necessary to combat it, especially hydrogen sulphite corrosion, which occurs when block containing slag or cinder aggregate are autoclaved. To offset corrosion, both types of racks have been increasingly made of solid bar instead of channel or angle stock. Special corrosion resistant steel and aluminum are also used. In some installations, racks are provided with wheels so they may be moved into and out of the autoclave as a train of cars. In a few plants, contour racks are even supported at the top by a monorail.
Frequent inspections have to be made for corrosion of the interior of the autoclave, particularly at the closed end and the bottom of the cylinder. Many plants do not remove aggregate particles and sludge as fast as they accumulate, and this accelerates corrosion and sometimes clogs the drains for removal of condensed, corrosive water. It is good economy to clean out the cylinder after each autoclaving cycle and also to see that the gaskets, lugs and all parts of the door sealing and safety mechanisms are clean and well lubricated.
Getting the block in and out of the autoclave is a time-consuming problem when it has to be done manually. Consequently several shortcuts have been devised in recent years, some requiring manual guidance and others arranged for various degrees of automatic handling. Lift trucks equipped with steel wheels which engage tracks running the length of the autoclave have been commonly used to move loaded racks in and out. The wheels are provided with rubber tires to cushion the trucks when they are run on the hard production floor to the autoclave. With the two-stage curing method, preset hardened block are usually cubed and placed on low flat cars which are wheeled on tracks in and out of the autoclave.
Autoclaved block are made from the same normal and lightweight types of aggregate (both natural and manufactured) commonly used for non-autoclaved block. Normal strength portland cement (Types 1 and 1A) are commonly used for autoclaved block. At some plants, high early strengths (Types III and IIIA) are used to provide block with enough early strength during the preset period to prevent distortion during the rapid temperature rise in the autoclave. Air-entraining portland cements (Types 1A or IIIA) are sometimes used to improve the molding and off-bearing characteristics and the resistance to freezing and thawing of block.
It has long been known that pure silica flour and some other silica-bearing or pozzolanic materials as fine as cement have an important effect on the strength and other properties of autoclaved concrete. During exposure to high pressure saturated steam at 120 psi. or more, the silica and lime from the hydration of cement go into chemical combination. With aggregates which contain no reactive silica-bearing materials, good results can be obtained by autoclaving block made with a mixture of about 60 per cent portland cement and 40 per cent silica flour. With aggregates which contain some fine reactive silica-bearing materials, the products manufacturer will need to determine for himself whether silica additions are desired and if so the exact proportions to use with
113
the particular aggregate, cement and silica flour available. A number of pozzolanic materials such as fly ash have been substituted, but some of these plants have returned to silica flour.
Although most of the autoclave plants are producing hollow concrete block, a number of plants have found that the quality, color and appearance of the solid masonry unit (split-block) is greatly improved by autoclaving. In a few sections of the United States, only autoclaved split-block can be sold, and plants making them are quite busy meeting the demand for this attractive masonry unit, available in a variety of colors. The improved dimensional stability obtained by autoclaving has virtually eliminated the former problem of shrinkage cracking in the completed walls, with fewer control joints. Autoclaving is also colorful. The characteristic lighter color of autoclaved block enhances the pleasing effects that can be obtained with dependable mineral colors in the mix. The batching, mixing, molding and off-bearing operations are essentially the same for autoclaved as for nonautoclaved block, with similar variations in the methods and equipment used.
Autoclave curing, as practiced by more than 200 plants accounting for well over 20 per cent of total block produced in the U.S. and Canada in recent years, promises to continue its important role in helping to provide for continuity and growth of the concrete block industry. Autoclaving has become a scientific, rapid, reliable way of curing that lends itself exceptionally well to automation and economical production. Hence, it has a very bright future.
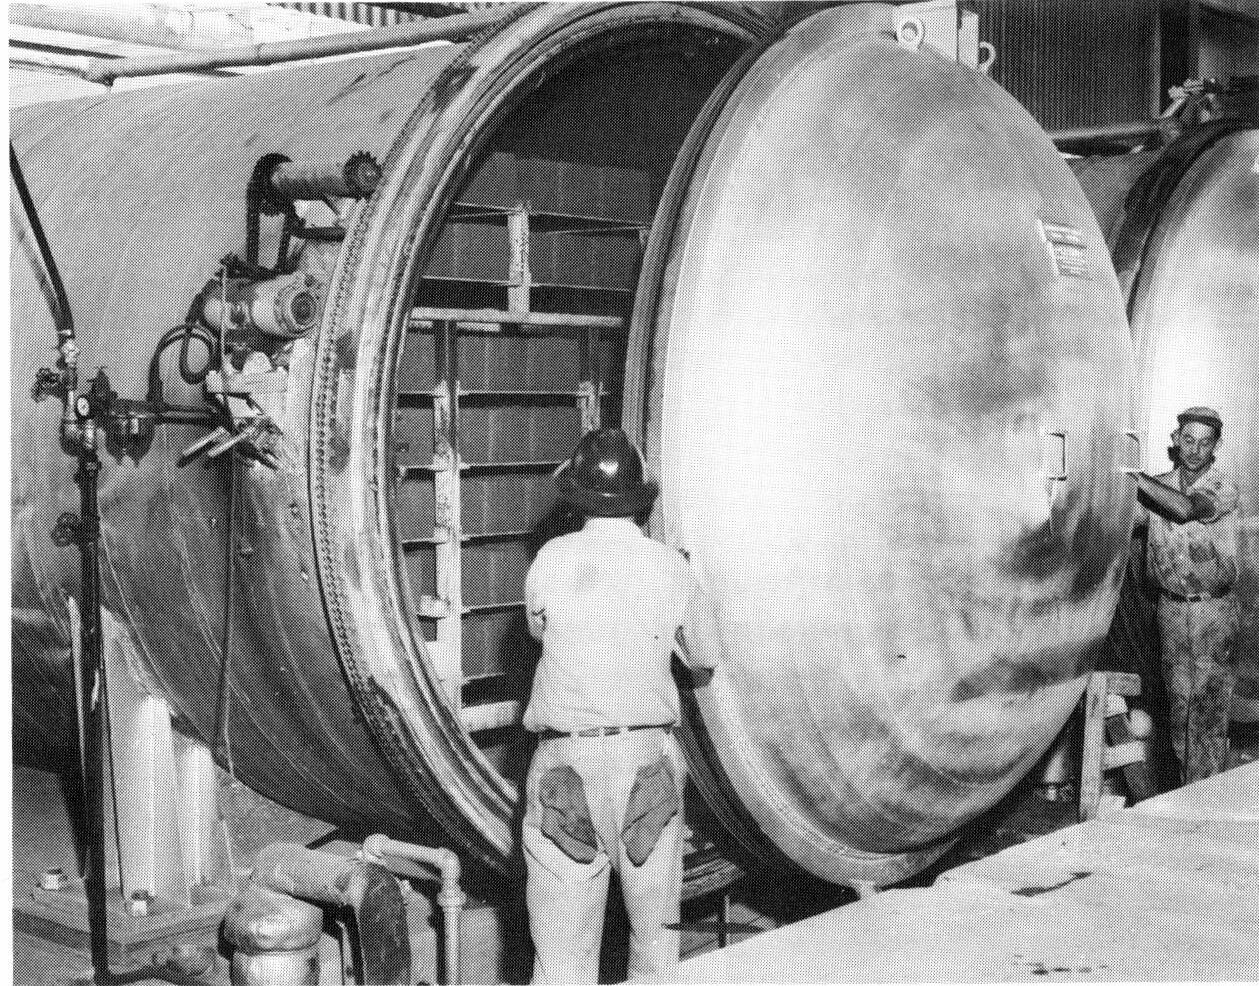
114
Quickclosing-opening Autoclave door.
Loading a bolted door Autoclave with a lift truck.
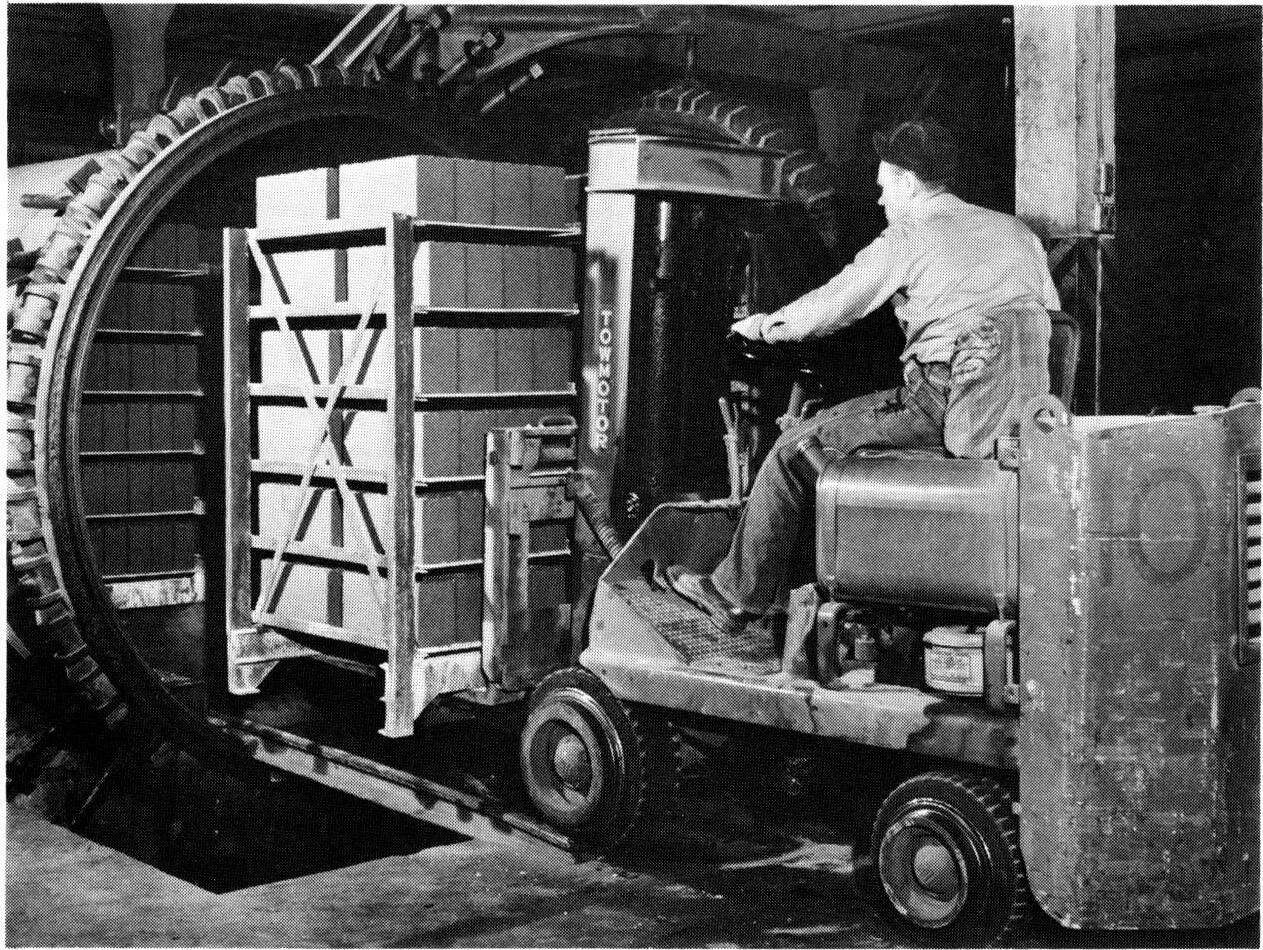
115
TheTransportationandHandlingof ConcreteBlock
By Earl Peterson
The beginning of the 20th Century brought a new industry and a new product called concrete block into the building market. With the birth of this new product to be incorporated in the building of all types of homes, churches, commercial and industrial structures, there was an urgent and immediate need to find a satisfactory means of transporting the block from the factory to the building site and for handling it at both ends. Seventy years later, these problems still vex the concrete masonry industry. They have challenged the ingenuity of the people who make block and service the industry steadily throughout the years and these people have responded with increasingly complex and sophisticated equipment to achieve their ends.
In the beginning any solution to the transportation problem was necessarily bounded by the only means of local transportation then available: the horse and wagon. Horses were as easy to obtain (and not quite as expensive) as trucks are today, but an especially strong wagon with large wheels was essential. It not only had to move steadily and easily on paved streets but also had to be able to navigate rough, unpaved roads that often turned into quagmires after a rain storm or during a Spring thaw. The biggest challenge was leaving the street such as it was and driving the horses over the rough terrain surrounding a building site. More often than not, the foundation blocks and mortar materials were the first deliveries to the job and they had to be unloaded as they had been laboriously loaded by hand, with the workman often standing ankle deep in mud or debris.
Usually one and practically never more than two loads comprised a day's work of eleven to twelve hours for the horse-and-wagon driver. Some delays were caused by the necessity of stopping the team at a watering tank, especially on the harder pulls. For some inexplicable reason, these tanks were usually located at the curb site in front of a saloon. This was probably the original "coffee break" as we know it today although the "coffee" then had foam on top and sold for a nickel.
Although this sounds terribly primitive today, one factor oddly enough has remained relatively constant since the beginning of our industry: the cost of delivery. The owner of a team at the turn of the century received two cents per 8 x 8 x 16" standard concrete block delivered to the job site. In a breakdown of this cartage cost, it was
117 XIII
more or less understood that one cent went to the driver for keep and maintenance of the wagon and the other penny was spent on feed for the horses. With two stout horses and a well built wagon, the average load was 80 concrete blocks weighing 50 pounds each or 4,000 pounds per load. Thus one horse could pull 2,000 pounds each working day.
When a block producer began to look over the local horizon, beyond the delivery range of the horse-and-wagon teams he could hire, the railroads came into view. Long before good, maintained roads and large trucks entered the hauling picture, early concrete block companies were able to use the railroads to enable them to serve a larger market. The Interstate Commerce Commission Rating Bureau allowed concrete block an already established brick rate and many producers took advantage of it to reach outside their local market area. One midwest plant, for example, developed a lumber dealer business of 300 customers who received concrete block by rail and this proved a most lucrative market between World War I and the depression years.
Most rail orders were shipped out in quantities of 800 to 1,200 units per carload. Usually an order would consist of about two-thirds plain or unfaced 8 x 8 x 16" units, with the balance made up of some type of face block either rock faced or bush hammered. During the peak of the golden years of the early concrete block industry, it was not unusual for a large plant to ship three to four carloads of block per day by rail. This manner of wide distribution influenced many lumber yards to discontinue their back-yard, hand tamped concrete block operations. Quality block shipped by rail proved more economical to the builder.
Gradually, however, during the 1920's, the United States built and paved its highways and developed the motor car the transportation of concrete block turned inevitably and permanently to the carrier that hauls virtually all of it today: the truck.
From the beginning, the uses of trucks for the transportation of concrete block were many and varied. For example, gravity dump trucks were used to haul sand, gravel and limestone chips to the block plants as well as delivering motor materials to the job site. Screened sand was usually delivered to the job on 8' x 12' flat bed trucks with drop sides or removable stack pockets. In the early 1920's dump trucks were first equipped with air or hydraulic cylinders to elevate the front of the truck bed so the material could slide off within seconds, thus saving many hours of unloading time, both at the plant and the construction site. A few years later, an important development by the General Tire Co. further expedited the truck delivery of concrete block. General replaced the hard rubber tire heretofore the only tire available with large, pneumatic tires that allowed trucks to go over rough and muddy terrain, thus enabling the supplier to put the concrete blocks where the contractor wanted them unloaded. Several truck manufacturers were quick to make the tire change, and it soon became a necessity in order to meet competition.
118
The evolution of truck sizes and loads has been a vital economic factor in the growth of the concrete block industry. Early trucks of all makes limited their loads to approximately 150 of the 40 lb. 8 x 8 x 16" units on a 8' x 12' flat bed. The truck wheel base, at that time, usually ran 156" from the center of the front axle to the center of the rear axle. But the concrete block industry was soon confronted with the different city, state and ICC rules covering how much of a load the truck could carry per axle, as well as limiting the gross load. The advent of dual tires finally became something of a life saver. Since they could be used on straight trucks, tractors and trailers, as well as on multiple axles under one truck bed. With today's average load of 720 to 1,000 standard 8 inch units on a single flat bed, one can readily see the importance of proper axle strengths, spacing and good dual and single tires.
Of the 500 or more car and truck manufacturers that have come and gone over the years, there are perhaps 15 models that stand out. One, now long gone, was the Republic one of the first trucks built to handle heavy hauling. Many of the early standouts are still active today and constantly striving to improve their products. Among the most popular heavy-duty trucks working daily at solving our transportation problems, International, Ford, GMC, Diamond T, White and Mack, would certainly be in the forefront and for those who need extra power coupled with economy, the Diesel Cummings engines are available in most heavy-duty trucks. Diesel engines usually offer much better mileage per gallon than ordinary gasoline engines, at about two thirds the cost per gallon.
Most concrete block manufacturers today lease out their hauling, although some rugged individualists both small and large operators find it more economical to own and operate their own fleets. These companies have usually instituted incentive safety programs for their drivers in an effort to hold repair and maintenance costs to a minimum; a typical program might offer two dollars to each driver whenever his vehicle passes periodic safety and maintenance inspections.
Getting the block from the plant to the building site is, unfortunately, only part of the transportation problem. They must also be transported to various pointsaround the plant as well as loaded and unloaded from the trucks. And over the years, these requirements have probably posed more problems, even, than the haul to the point of construction.
As mentioned earlier, in the horse-and-wagon days concrete block had to be put on the wagon one at a time by hand. And material handling around the plant during this same period was almost as primitive. The first significant examples of progress in this type of equipment were the end and gravel bins designed to discharge into the mixer, which had been elevated sufficiently so the concrete could be discharged to a platform from which it could be shoveled into the molds. Where the contour of the ground made this impossible, pioneer producers obtained about the same results by coming up with inclined belt conveyors. The first mechanical advance in loading and unloading block was the use of steel rollers 12" wide and ten feet long that could be used in series, thus making gravity conveyors that saved thousands of steps per day. Also, two-wheel upright carts were adapted to wheel block either on or off the truck or to yard storage.
119
However, these devices for handling raw materials efficiently caught on very slowly. Mechanized material handling equipment was uneconomical for the vast majority of plants which were too small either to finance or utilize it effectively. In practically all plants in the early years of the block industry, material was handled too often and lifted too many times and little thought was given to efficient plant layout.
The same shortcomings existed for many years at the construction site, which has long been the focus of the major headaches of material handling for the concrete masonry industry. Unloading techniques have always been an important competitive consideration, taxing the manufacturer's ingenuity in figuring better means of serving the customer at the job site.
From the beginning of our industry, producers have been trying to place the block on the job where it will be most convenient for the mason-bricklayer. For many years, the deliveries were made as close to the wall line as possible. If the job happened to be a basement, the driver might throw the block in the hole, where a mason's helper would stack them around the footings. Or he might slide the block down a plank into the hole. Often, however, a job site was so muddy that the truck couldn't get near the foundation. When that happened the driver might have to carry his load by hand, two-at-a-time, a hundred yards or more to the job in order to make a correct delivery.
Although this situation improved slowly, it wasn't until after World War II that the concrete block industry realized that in order to keep good employees, it would have to mechanize its operation in the areas of both production and delivery. At that time, for example, very few plants throughout the country had paved storage areas over which fork lift trucks could operate. In some states notably Florida, the Southern Gulf region, and California there were sandy conditions that created about as much of a problem as rain and frost in other areas. All of this began to change in 1946, when Towmotor came out with large, 8:50 x 15 pneumatic tires that enabled the manufacturer to stack his block wherever he wished. While this bit of progress was still catching on with block manufacturers, customers began complaining about cubes of concrete block that had been stockpiled on dirty or muddy areas. Stains on the block were very noticeable when the block were laid in a wall. The hard surfacing of stockpile areas corrected this situation. It also allowed the block to be piled higher, and reduced chips and cracks by making possible more careful handling.
Once the economics in such improvements were evident to the block producer a whole sequence of equipment to help him handle his product appeared on the market. Some of it caught on and some didn't. For example, in the early 1950's, an ingenious unloading device was developed that featured an 8' x 16' flat bed floored with rollers. A hydraulic lift under the floor elevated the front part of the loading bed. An entire load of 850 standard block would gradually roll down the truck bed. The load was restrained from tumbling too fast by a powered winch. As the blocks touched the ground, the driver would inch forward, making room for each new row.
120
Another device won great popularity in Florida and California particularly. A 4,000 lb. capacity lift truck would be coupled to the rear of the delivery truck when the driver started out with a load. At the job site the driver would spot his truck, unhook the lift truck and use it to unload. Although the idea was workable, it probably failed to sweep the country because it required the contractor to develop an area for unloading and not very many contractors were willing to do this.
About the same time, another invention appeared that received immediate acceptance throughout the block industry. The Superlite Company of Phoenix, Arizona, developed an economic (less than $2,000) unloader that came to be known as a straddle-type. Shaped like an inverted U, the straddle-type unloader would be secured next to the cab when the truck was loaded. It was self-contained, and powered with a Briggs & Stratton 10 h.p. gasoline motor. The whole unloading unit was self-propelled and would move along the truck bed on rails, setting the block down on the ground or lowering them into a basement. It's main limitation was a lack of versatility; it could only unload to the rear of the truck.
It was this limitation in part, at least that inspired the development of the boom truck in the mid 1950's. Probably no single piece of equipment has revolutionized block handling as much as the boom truck for job site unloading. Because boom-type unloaders operate in a complete sphere of 360°, they can be used to put a pallet of block or mixing materials almost anywhere a mason or contractor instructs the driver to unload.
There are a half-dozen manufacturers of boom trucks, and prices are quite competitive. Cost is usually determined by the buyer's needs. Booms started with a radius of 18', but many are now made to reach 24', with a small inner cylinder that can add two more feet when necessary. Because the cost of an average boom with special truck bed and installation may run as high as the cost of the truck from $9,000 to $11,000 many block plants are limited in the number of booms they can own or contract. The versatility of boom trucks has influenced some contractors to demand extra and unpaid services from the driver; whether or not he gets them, usually depends on competitive conditions.
Trucks mounted with booms can haul about 120 concrete blocks on an 8' x 18' flat bed; if the load is standard lightweight units, the haul increases to about 1,000 blocks. A pup (one axle trailer) can also be attached to the rear of the truck to haul an additional 300 concrete blocks or 450 lightweights. The maximum load for over-theroad, under ICC regulations, is 1,600 lightweight 8" x 8" x 16" standards.
In an effort to expedite material handling and provide block to the job site in the best possible condition, block producers have recently taken to piling their merchandise on wood pallets, a refinement both neat and effective that is also threatening to turn on the producers economically.
121
Most pallets are made of 2" x 4" wood stringers faced top and bottom by 1" x 6" boards, four feet square. The price averages about three dollars per pallet, plus normal overhead charges. The average wood pallet seems to have a life of three trips, mainly because it is badly mistreated on the job site. Hence the cost of pallets even though they offer many advantages in product delivery has become a major economic factor to producers. Recently, some block manufacturers have begun to charge contractors five dollars apiece for wood pallets destroyed on the job site. Unless this practice extends pallet life, the use of pallets may well have to be discontinued at a sacrifice in appearance of the product in the finished structure.
This, however, is a minor detour when placed alongside the remarkable progress made over the two decades since World War II in the handling and transportation of concrete block. Today, the unloading time of a truck has become a few minutes, as contrasted with the three-quarters-of-an-hour it took when done by hand. Paved yards offer a clean, fast surface for mechanized plant equipment, and truck booms put the product wherever the customer wants it on the building site. As a result, the yard help and the drivers are more productive and happier and so, apparently, is the customer.
The only dependable means of local delivery in the early days was by horse and wagon. A wagon like this, drawn by two strong horses, could haul 90 plain or rock-faced units on each load.
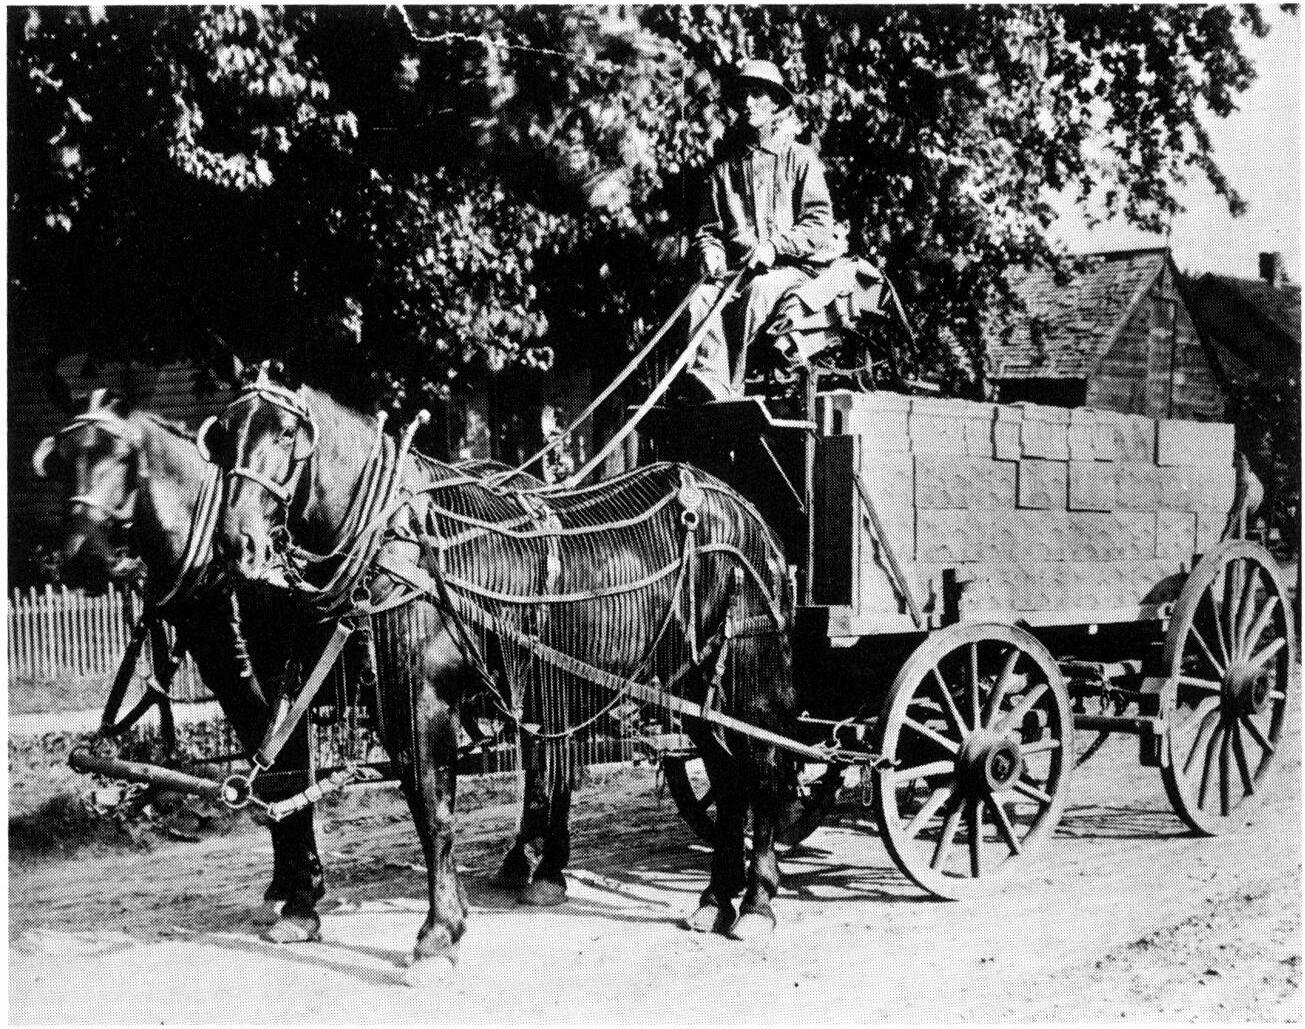
122
This fleet of Republic trucks was delivering concrete block in 1922. Each truck could handle about 180 standard blocks per load. Tractor andsemi-trailer trucks began to appear in quantity for hauling concrete block soon after World War II. They hauled loads between 600 and 950 standard blocks. The ultimate today in the transportation of concrete block is the boom truck pulling a tandem pup trailer. This permits a pay load of 1,200-1,600 block that can be unloaded wherever the contractor wants them on the job site.
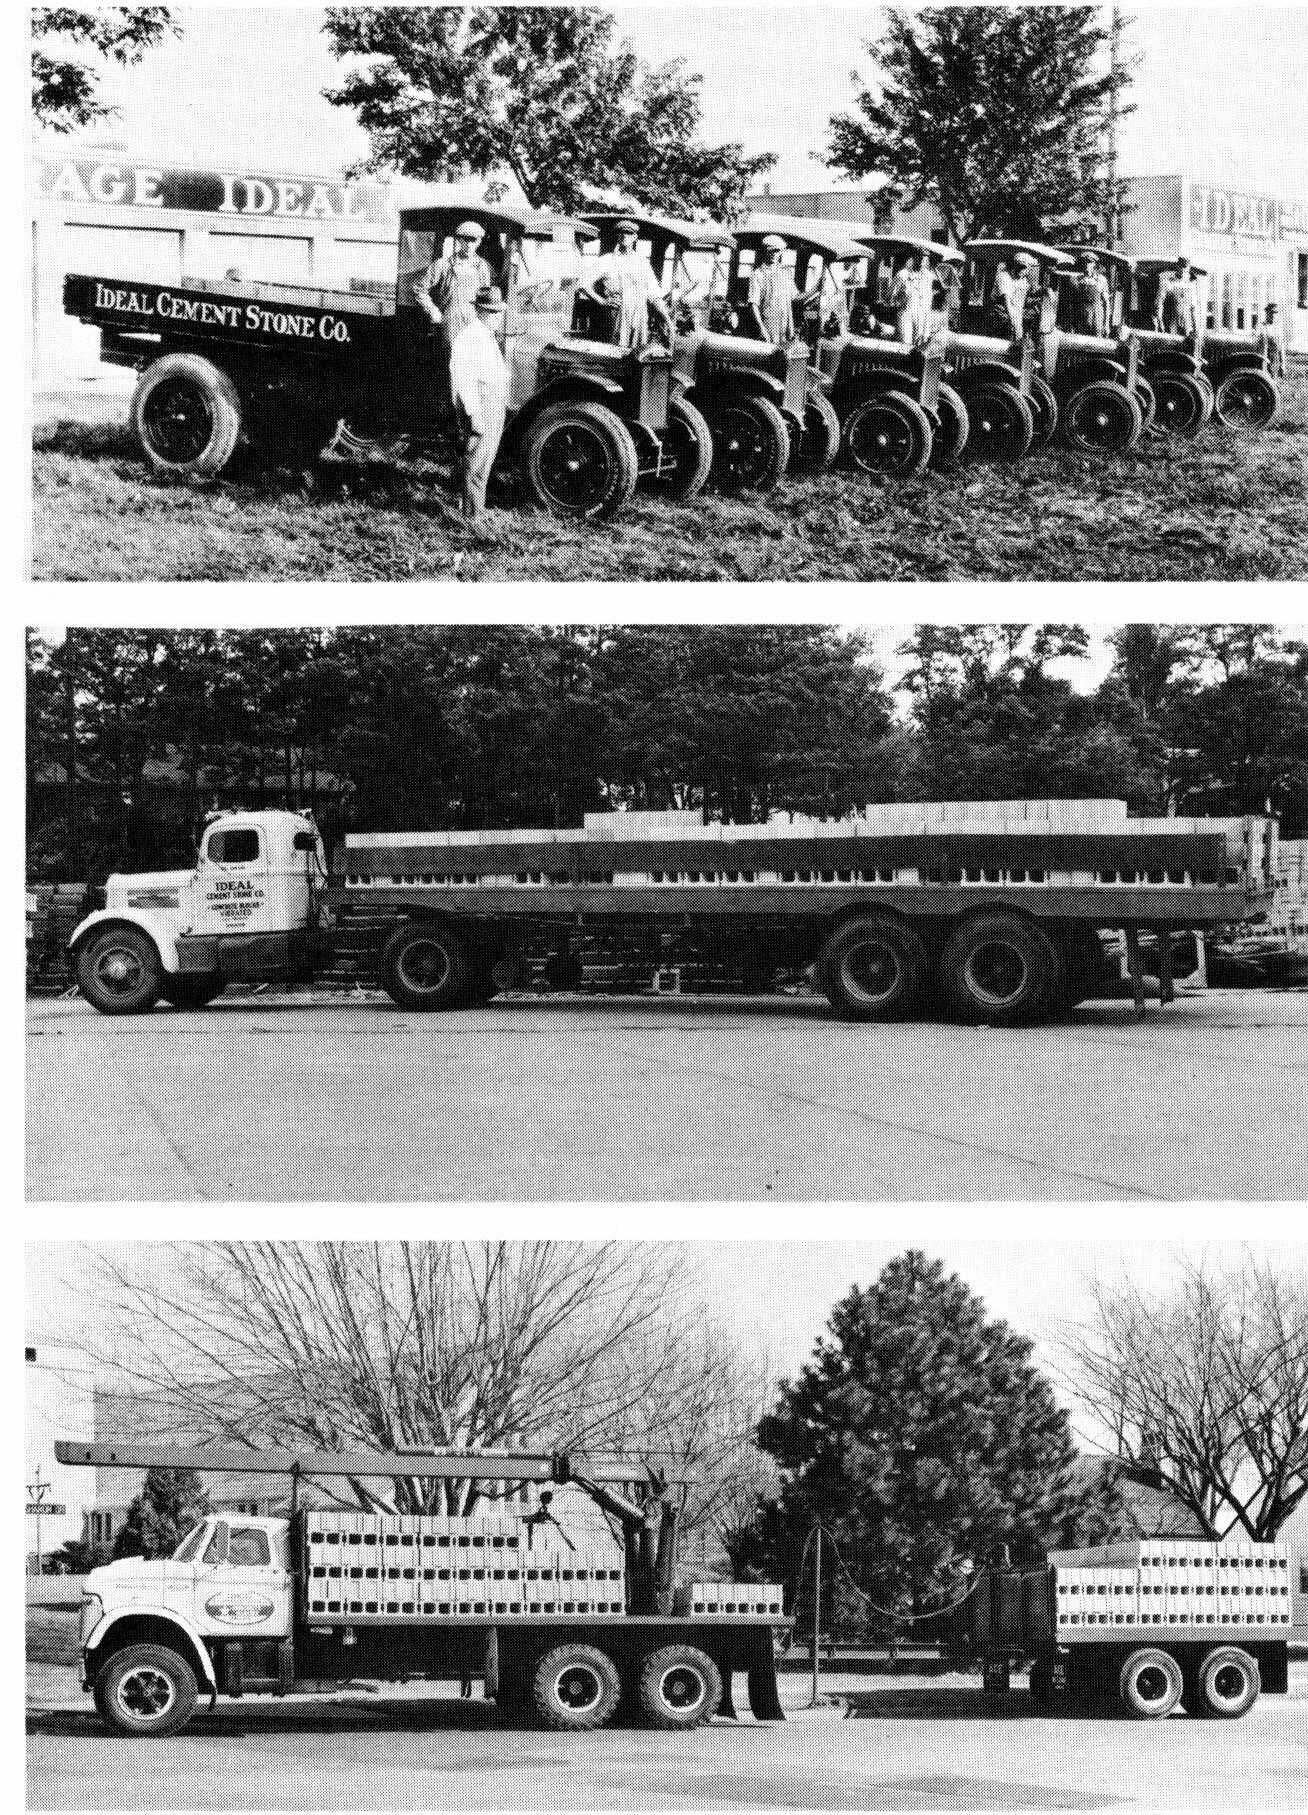
123
The Evolution of Concrete Masonry Machinery
By Eugene F. Olsen
In 1890, an industrial pioneer named Harmon S. Palmer began tinkering with a machine for making concrete block. Ten years later, he patented the basic principle of the hollow concrete block machine with removable cores and adjustable sides and an industry was born.
There were some serious bugs in Palmer's machine. It produced block so large and heavy they had to be derricked into a wall. Thus job site production was highly desirable. Palmer's machine was relatively simple, with a lugged mold box with movable side plates and cores, and a removable bed plate. A dry mix was shoveled into the mold and rammed by hand. By turning the hand crank the tapered cores were withdrawn, and the sides were opened. The block were dried until they could be stood on end in a stock pile, pallets were removed after 24 hours, and the block were protected from the sun by an improvised shed placed over the pile.
Two men were able to produce 80 blocks per day, five men, 200 blocks per day. The unit cost was 19¢, broken down as follows: cement, 12¢; labor, 5¢ and sand, 2¢. Although overhead, transportation, and other expense were not taken into consideration, they would have been insignificant at that time.
The Palmer machine was advertised as being capable of making a variety of plain and ornamental block and Palmer was especially proud that a leaf could be inserted within the mold box for pattern effects. These block had a 40 per cent air space and it was claimed that the inside wall was so smooth and free from moisture that wallpaper could be applied directly. Even though they were also distressingly porous, the building department of the city of Chicago in 1897 approved the construction of six buildings made from Palmer's hollow concrete block.
Palmer sold his machine for $200 on a royalty basis with exclusive territorial protection. In 1902, he incorporated the Hollow Concrete Building Block Company in order to establish plants for the manufacture of block machines, and by 1904, he hadproduced 400 machines.
At the same time, there began to appear on the market a number of other block machines, all of the hand tamp variety, with changes only in detail from the Palmer design. The intense competition that developed has
124 XIV
continued to the present, leading to much of the progress in concrete masonry equipment over the relatively brief life of this basic industry.
The heart of this competition is, of course, the block machine, itself. Therefore, any history of concrete masonry equipment can best be divided into the four rather distinct periods dictated by the advent of basic revolutionary improvements in block machines: the hand tamp era; the power tamp era; the automatic tamp era; and the vibration era.
Hand Tamp Era: 1904-1914
Before Harmon Palmer, the few preformed concrete masonry buildings in existence were constructed of building units formed by hand or in such wooden forms as soap boxes, similar to the manufacture of the sun dried mud units known as "Adobe."
Then came Palmer and his machine, and with it the beginnings of the hand tamp era of concrete block manufacture. Palmer's success invited imitation, and he spent much of his time trying to track down competitors who were stealing his process. He had a standing offer of $5 reward for information about any person who made or laid hollow concrete block without his permission, and he filed and won a number of suits for patent infringement. But finally the avalanche of imitators overwhelmed Palmer. Within a few years of his first commercial machine, there were more than a hundred competing machines on the market, and bringing them to heel became an impossible task.
These often fly-by-night machine manufacturers dangled wild claims of fortunes to be made in concrete block and attracted hundreds of incompetents into the business. Some of the equipment producers published advertisements and literature estimating the cost of manufactured block with their machine, of course, at less than the cost of the cement, alone, needed to produce a quality unit.
In 1905, for example, one block machine advertisement printed in the Scientific American stated that block costing 6¢ to make could be sold for 18¢, and that the entire machine cost only $125. In other words, it was claimed that a daily profit of $20 could be made on an investment of only $125. Salesmen were even more extravagant in their claims. "You can buy a machine," quoted one "start making block on Monday with two men, have another man commence laying the same block on Tuesday and have them all laid in the wall inside of 24 hours after they are made."
Such claims encouraged the uninformed and inefficient producer to enter the block business, and the result was a poor product that ruined business for the good as well as the poor producers largely because of the influx of a handful of greedy or unscrupulous manufacturers of block machines.
125
The machines described under dozens of different trade names in the construction publications of that day were predominantly of the "down face" type in which the mo ld was turned on its side to facilitate facing (See Figs. 81 and 82).
The down face technique permitted the use of a richer, drier mix for the face of the block, and such faces were usually formed in rock, panel, bush hammered or similar designs. The cores were of various shapes and number not unlike present day block. However, the face shells and cross webs were much thicker, and blocks were heavier.
A number of other types of machines in addition to the down face were being produced. They can be grouped roughly into three classes: upright, wet process, and two piece.
The upright machine for making hollow block consisted of removable hinged sides and upright interior cores, and block were made by tamping under the dry process. In one common upright type, known as the roll-over, the plate to which the two cores were attached was set on a table; the plates comprising the sides and ends were selected according to the particular design desired for the surface of the block and were clamped into place. The material was tamped as it was added to the mold, and the top of the mold was leveled off. Then a board was placed on top and this entire apparatus turned over so the mold rested on the board. The plate to which the cores were attached was then removed, the sides of the mold taken off, and the block carried away on the board for curing.
The machines operated by the wet process used many types of molds. Some molding was done in sand, some in wood, and some in a system of sheet-iron molds. Sand molds were similar to those used in a foundry, while the wooden and iron molds had interior cores. The wet mixture was simply poured into the molds and allowed to stand for several hours.
Two piece block machines were used for making block for two piece walls. Such block provided a continuous horizontal air space, with more thorough insulation than that offered by one piece block. It was also easy to make; since each block had only one face, the interior cores were eliminated and it was possible to make the block under direct and instantaneous pressure without any need of a tamper. Two piece block were manufactured by a mechanical press, using a medium wet mixture in which coarse aggregate was employed.
Most of these early hand tamp machines could make various sizes of block. The height and width ranges were much the same as now (except only one-quarter inch was allowed for mortar joints). The popular lengths, at first, were 32 and 24 inches, but this gradually dropped off to 20 inches.
126
Early day advertisements of concrete block machines make fascinating reading. Among the more prominent companies and machines advertised in this period were:
Zagelmeyer Cast Stone Block Machinery Co., Bay City, Mich. concentrating on racks, each holding forms for twenty blocks, into which slush concrete was poured.
Hobbs Concrete Machinery Co., Detroit, Mich.; whole principal product was a hand tamp machine making ten bricks per operation.
W. E. Dunn Manufacturing Co., Chicago, Ill.; maker of a down-face block machine and ornamental molds.
Ideal Concrete Machinery Co., South Bend, Ind.; another manufacturer of popular down-face block machine.
Anchor Concrete Machinery Co., Rock Rapids, Iowa; Specializing in a continuous air space block machine.
Besser Manufacturing Co., Alpena, Mich.; whose down-face machine, called Eureka, was the forerunner of a wide variety of block machinery.
A closer look at three of these companies will give a better view of the equipment manufacturing industry in the early days of concrete masonry. In 1910, the Zagelmeyer Cast Stone Block Machinery Company of Bay City, Michigan, actively began to merchandise its "slush method" of making block. A soupy wet mix was run out of a mixer through a chute into metal molds which were placed on a car on tracks. At first, each mold made 15 block, later the number was increased to 20. The concrete was roughly leveled off and allowed to set for one hour; then the block were troweled slightly and shoved into a curing room, still on the same car. When the block were cured with dry heat, the cars were pushed out into the yard, unloaded, and the process repeated. Dry heat was used because the block had too much water in them when they entered the curing chamber. This was in sharp contrast to the block made by other methods, which were usually much too dry and needed all of the moisture they could get during the curing process.
The Fisher hydraulic block machine came out in 1910. The mortar was rammed by heavy pounding driven by a two-plunger hydraulic pump displacing the air and bringing the aggregate together. Around the center strain rod was pinioned a table mounted on wheels. On this table were fastened three mold boxes that rotated from the filling table to the press to the delivery and then back again to the filling table, making it possible
127
for all three boxes to be in operation at the same time. It was claimed that two men could produce between 1,000 and 2,000 block a day on this machine.
The Besser Manufacturing Company of Alpena, Michigan the largest single producer of block machinery today designed several important types of block machines during this early period. The company was founded by a Michigan lumberman named Herman Besser, who started manufacturing cement when timber sources were dwindling, then branched into concrete block and, a few years later, into machinery for making concrete masonry units.
From the very start, the founder's son, Jesse H. Besser, president of the company, devoted the major share of his time to the development of improved designs of block making machines. By 1909, the company was able to offer block makers a power tamper for working over the hand machine and in 1913, Besser came up with a continuous mixer designed to eliminate serious criticisms against former makes. One of the main objections had been that the time of the mixing was mechanically determined. In the Besser mixer, all operations were continuous but the machine could be instantly stopped or started as desired, and it could be operated at any percentage of capacity up to the maximum. It was claimed that if the hoppers were kept full, the machine would automatically continue to measure, proportion, mix, weigh, and discharge the concrete.
A year later, Besser brought out a single automatic down face block machine with a claimed capacity of three block per minute, indicating the gradual early increase in the productivity of block machines.
While this period was predominantly one of tamping the concrete by hand, it was apparent for several years that the era of universal power tamping was approaching. As early as 1906, the Kramer Automatic Tamping Machine was being advertised and the power tampers introduced by Besser, Ideal and Anchor in succeeding years insured the ascendance of this type of equipment.
The Power Tamp Era, 1914-1924
The early power tampers although mechanically rather crude were a vast improvement over hand tamping. They sharply reduced the cost of concrete block while improving the strength, uniformity and general quality of the product. In most power tampers, bars or rods were lifted by either chains, cranks or cams and dropped by gravity. They were activated and stopped manually, and uniformity depended on the machine operator. About half of the tampers lifted all the bars or rods at once; the others lifted alternately. Some power tampers were also suspended over the block machines, while others stood on the floor, straddling the machine.
128
It was during this period that the concrete building tile a 5" x 8" x 12" thin shell and web unit was introduced and became quite popular. Machines for making concrete tile were closely similar to the block machines and were offered by most of the block machinery manufacturers.
Marginal equipment manufacturers were finding the going tough, while the stronger entries continued to grow and prosper. Kent Machine Co. of Cuyahoga Falls, Ohio entered the field with an attractive line of equipment. Otto Walter of Perrysville, Indiana backed a strong promotion job for concrete roof tile with a quality tile machine. Universal Tamping Machinery Co. of Peoria, Ill. began to come on strong and the Helm Brick Machinery Co. of Cadillac, Mich. came up with a brick press that turned out a handsome unit.
The Anchor Concrete Machinery Co. moved in 1922 to Adrian, Mich., where it purchased a modern factory, including the business of the Hobbs Block Machinery Co. Blystone Manufacturing Co. of Cambridge Springs, Pa., introduced a modern automatic hydraulic machine for the manufacture of 5" x 8" x 12" inch concrete building tile. The W. E. Dunn Manufacturing Co. moved fromChicago to Holland, Mich., and Ideal Concrete Machinery Co. moved to a modern plant in Cincinnati.
During this period, the size of concrete units was being standardized. This, of course, was a tremendous step forward and expedited more general acceptance of concrete block.
About 1912 the first "stripper" block machines came on the market. This type got its name because the mold boxes were rigid (not unfolding, as with down face machines), and the packed block was extruded stripped from the mold. The early strippers employed "cored" pallets which were dropped into the top of the mold, the concrete was tamped, and push rods then engaged the bottom of the pallet to strip the block from the rigid mold. A separate set of pallets was obviously required for each shape of block to be made. Such pallets were made of cast iron or pressed steel.
During the "Power Tamp Era" especially between 1920 and 1924 most of the leading block machine makers (Besser, Ideal, Anchor, Kent) introduced stripper machines, of roughly similar size.
In 1924, as a direct result of the engineering development work of Jesse Besser, the company brought out one of its most important contributions to the block industry the first successful stripper machine using plain pallets. The Senior Automatic Plain Pallet Stripper, as it was called, marked a revolutionary advancement in the art of producing concrete masonry units. By making it possible to produce any size or type of unit on the same steel or wood pallet, it greatly reduced the producer's initial investment and operating cost, and opened wide new opportunities for the industry.
129
With the exception of pallet feeding and the removal of finished blocks, the machine introduced in 1924 was fully automatic. For the first time cores were supported from above, and the blocks were stripped by the upward movement of the mold against a stationary stripper head. This machine operated at 6 cycles per minute, producing about 800 units per man-day.
Although the plain pallet was probably the most important single development of the power tamp era, E. N. Goodlett of Chicago was experimenting with a wave of the future during this same period, and in 1919, the Goodlett Vibrator came on the market. It was the first device employing the vibration principle to be marketed in the United States. The Goodlett Vibrator consisted of a double frame with a power driven shaft and pulley connection. Molds were filled with concrete and placed on the upper frame. Vibration was produced by the reciprocal movement, in a horizontal plane, of the upper mold bearing frame, which was supported over a fixed lower frame. The amount of agitation of the mold could be regulated by adjusting either the length or frequency of the stroke. The Goodlett Vibrator was almost two decades ahead of its time, but the promise it offered was very real.
Automatic Tamp Era: 1924-1938
This was a transition time in the machinery field (Fig. 83), when gains were being consolidated and the bugs were being worked out of ideas already gestating. It was primarily a time of improvements and refinements in the power tamp machines in general use since the end of World War I.
Slowly, in small increments of skill and power, machines were better and more heavily built, with a steadily higher degree of automatic operation. At last, Besser, Anchor, Kent and Portland all broke through with completely automatic, high production block machines, capable of daily capacities up to three thousand or more 8-inch equivalent block per 8-hour day. Other manufacturers were pushing ahead in similar directions but the changes were not all technological.
In 1927, a new company called Consolidated Concrete Machinery Corp., was formed in Adrian, Mich., the result of a merger of five important existing firms: Anchor, Ideal, Universal Tamping, Adrian Steel Casting, and the Thomas W. Noble Co. The new company was headed by Eugene F. Olsen, who had been president of Anchor. In 1931 a controlling interest in Consolidated was purchased by Besser Manufacturing Co. of Alpena, Mich., and the operation was moved to that city. In 1932 Consolidated was dissolved, and Olsen organized the Stearns Manufacturing Co. in Adrian, Mich. to manufacture and sell concrete block machinery.
130
Much of the progress that might have been made in concrete block equipment during this period was stifled as was so much in all of American society by the Great Depression, which hurt the concrete products industry grievously just when it was beginning to get well on its feet.
And so the automatic tamp era became a period of bits and pieces of progress, bounded always by the economic restrictions and the devastating disenchantment of the depression years. There were mostly embryos waiting for the right time to be born. And that time didn't come until another Great War pulled America and the world out of a Great Depression.
But while they awaited that right time, the ideas grew and formed. And the most potent idea of them all and probably the most important single development in the history of concrete masonry machinery was the introduction of automatic, high capacity vibratory block machines.
Vibration, a principle which was to revolutionize the concrete block industry about 30 years late, was first introduced in England in 1910 in the production of heavy monolithic block, piles, girders, and similar heavy concrete products. The Improved Construction Company of London brought out an oscillating and vibrating table on which molds were placed (called the Jagger Process, after its inventor, P. B. Jagger). A horizontal vibratory motion, together with a sudden arresting rocking movement of the table supposedly brought about a rapid solidification of the particles, packing the aggregates closely together and reducing the percentage of voids. It was many years before this vibration principle was applied to the manufacture of concrete block, but when it was, it became a vital contribution to the growth of the industry.
The Vibration Era: 1938-1970
A decade before the start of this era, a Californian named Stephen Flam was making building tile in a machine which packed the concrete by vibration and stripped it from the mold immediately after packing. The units were only 31/2 in. high with thick shells and had to be used with a wet mix. But Flam felt that if it were possible to pack units of standard 8-in. heights by vibration, such a process might have a great future.
About the same time, Louis Gelbman, of Yonkers, New York, who had studied the successful use of vibration in the placement of poured concrete structures, also decided that this principle could be used to pack concrete block. So Gelbman designed a block making machine in which the mold was periodically vibrated for short periods of time to insure complete packing. Gelbman applied for a patent in 1928, and it was granted to him on June 4, 1935. He continued to improve his machine during this period and his efforts finally resulted in the development of a completely automatic block machine. However, Gelbman found it difficult to merchandise a high capacity machine in the middle of the depression, so he introduced a smaller machine, which produced only one standard block at a time. This machine was on the market only a short time when the Steams Manufacturing Company of Adrian,
131
Michigan, was given exclusive sales and manufacturing rights for it in 1934. Gelbman and Stearns worked together in further improving this machine which they called the "Joltcrete." The first small model was shown at an exhibit of the National Concrete Masonry Association in Detroit in 1936, and the following year a much higher capacity and automatic vibration machine was given a road test at National Cement Products Co. in Toledo.
The Stearns Joltcrete vibrator applied the principle of limited amplitude vibration under pressure the mold box being stopped in both up and down positions so the limited travel subjected the material to 7,200 packing blows per minute. There was a 15 second vibration cycle, and the mold box traveled three sixty-fourths of an inch in a vertical plane. Three standard 8 x 8 x 16" concrete blocks were produced at one time on the large Joltcrete, and its rated capacity was nine to 11 blocks per minute. Other sizes could be manufactured by making the proper adjustments. In addition to the inventor, the persistence and skill of Arthur B. Mays of the Steams Co. was primarily responsible for the success of this revolutionary development.
In 1939, several other vibrating block machines were introduced, including the Besser "Vibrapac," the Multiplex "Mufti-Vibrator Press," and the Kent-Root "Vibra-Press." Of these machines, the most popular was Besser Vibrapac licensed under both the Gelbman and Flam patents. The Vibrapac Machine had a rated capacity of 10 standard 8 x 8 x 16" concrete block per minute and made three standard units at one time on a single pallet.
These vibrating block machines increased the labor productivity per man day from about 200 to as high as 600 block. Regardless of the nature of the aggregate used, vibrating machines gave promise of producing a better textured face, sharper corners and generally a better quality product than the average tamped block.
With the advent of this practical machine, however, a great controversy arose in the industry as it always does with any revolutionary innovation as to whether tamped or vibrated blocks were better. Most members of the industry, including block men and block machinery manufacturers, took sides.
In an effort to determine the relative merits of the two processes, impartial tests were conducted at the University of Wisconsin. These tests, and the subsequent published report, became popularly known as the "Wisconsin Tests." The net results of these tests were highly favorable to the vibrated block so favorable that all the major machinery manufacturers and, subsequently, the block manufacturers, gradually converted to the vibration principle, and vibrated block had complete acceptance.
The advent of the vibration era gave additional impetus to the use of lightweight aggregates because the vibration machines handled such aggregates better than the tamp machines had. Packing the molds by vibration not only resulted in greater strengths, better textures and uniformity, but also increased production tremendously. Even more importantly, it facilitated making block machines fully automatic, (Fig. 84) and this, in turn, led the way to automating the placing of green blocks on curing racks or into curing chambers.
132
Automatic Rack Loaders-Unloaders appeared on the market in 1953. Promptly after that came mechanical block Cubers, in models varying from mechanical aids, to semi-automatic, to fully automatic. These incorporated devices to turn units around and/or over by 90 degrees or 180 degrees. Some will cube any desired interlock pattern.
During the Vibration Era, the concrete masonry industry gradually automated the other equipment required in a block plant. This, to a high degree, was accomplished through equipment manufacturers who developed such items as Mixer Automation Systems, Automatic Rack and Car Movers (both in and out of curing kiln), delivery truck mounted power cranes for loading and unloading cubes of block, and other ingenious labor-saving devices.
In a number of block plants in the United States and Canada, automation is now so complete that they are virtually "Push Button" operations. In this way labor costs have been held within workable limits in spite of steadily increasing pay rates.
After 50 years of remarkable progress in block plant machinery to the point of total automation it would seem that the optimum has been approached. But if there is any lesson in history it would have to be that there are new ideas and new developments, beyond even our imagination today, yet to come.
A list of the major machine manufacturers for block plants in the United States in 1969 would include the following (in alphabetical order)
Bergen Machine & Tool Co., Nutley, N.J. Besser Co., Alpena, Mich.
Builders Equipment Co., Phoenix, Ariz.
Columbia Machine Co., Vancouver, Wash. Gocorp, Inc., Adrian, Mich. (Successor to the Gene Olsen Corp. in late 1965)
Kent Machine Co., Cuyahoga Falls, O.
The Lithibar Co., Holland, Mich.
Praschak Machine Co., Marshfield, Wis. Stearns Mfg. Co., Flat Rock, Mich.
This Miles Number One Block Machine is typical of the "downface" block machines in the early years of the hand tamp era. Wood pallets were
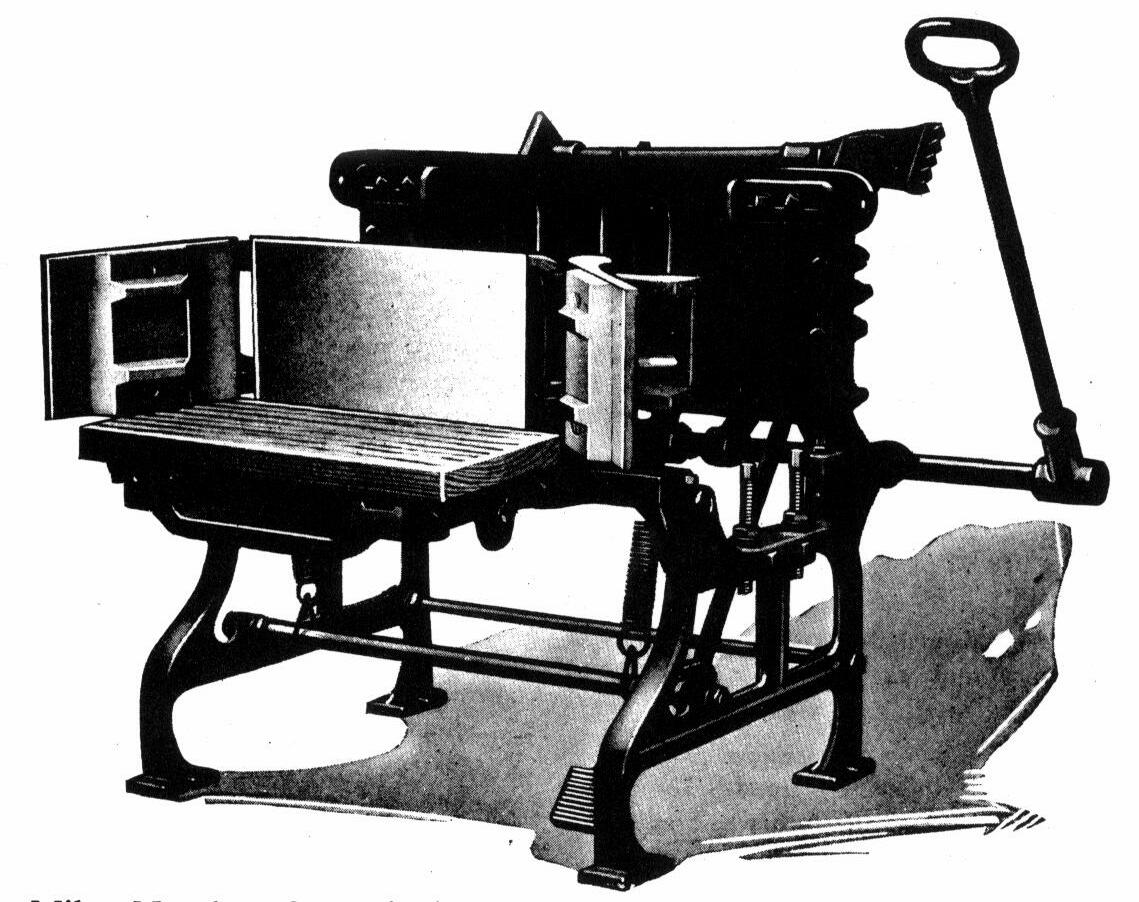
133
This block plant view is typical of the first few years following the advent of the high production vibration block machine.... In the foreground is a "three-at-a-time" machine, and beside it, a tamp type power stripper. Also in view is a downface block machine under a power tamper, emphasizing the transition period.
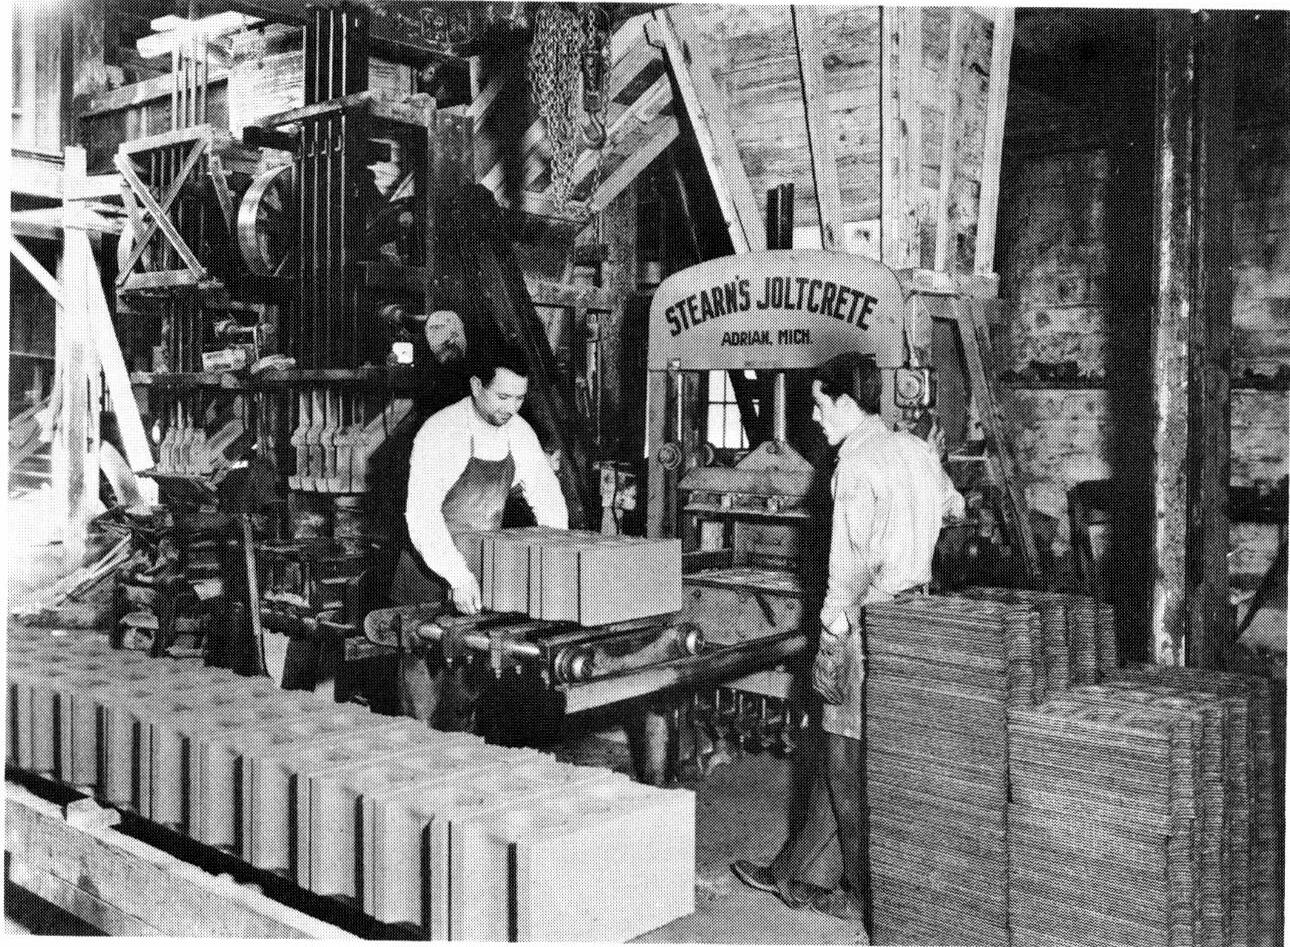
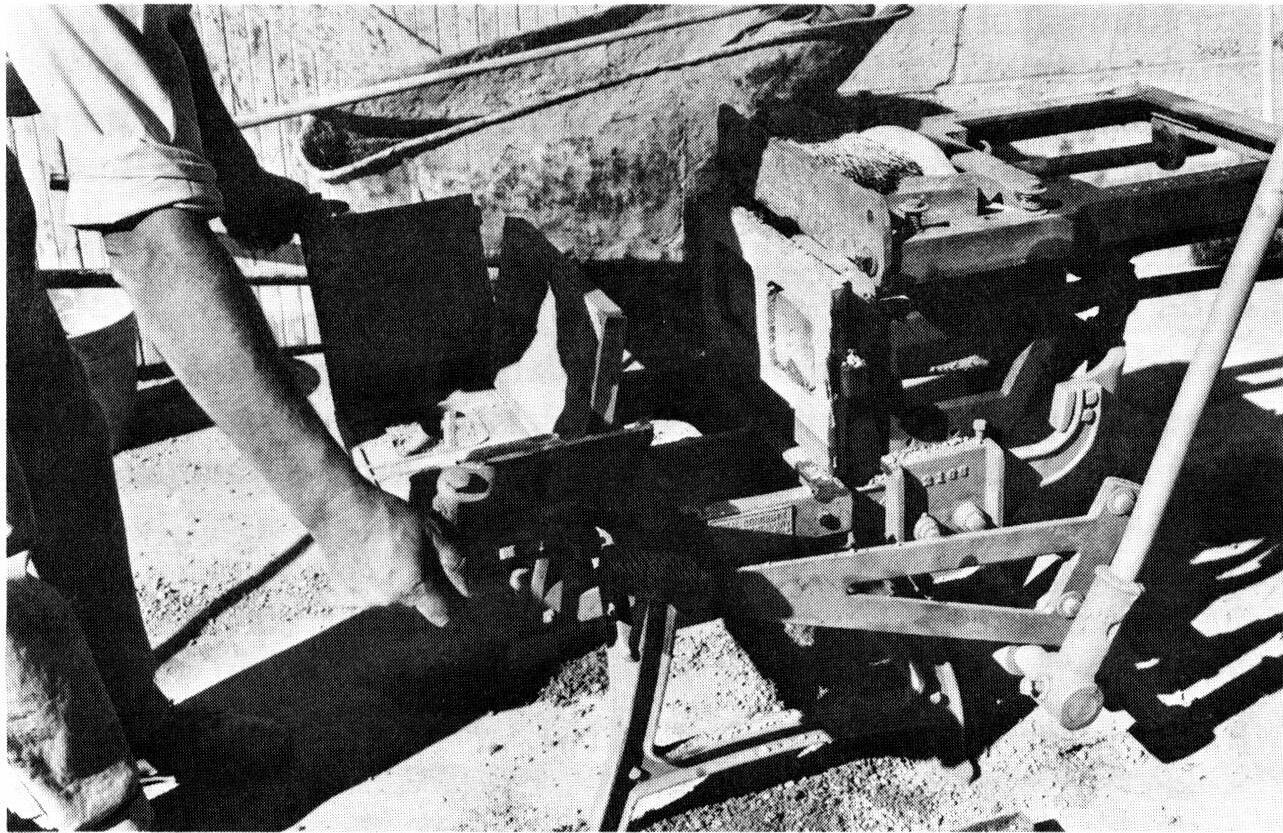
134
Another example of an early downface hand tamp block machine.
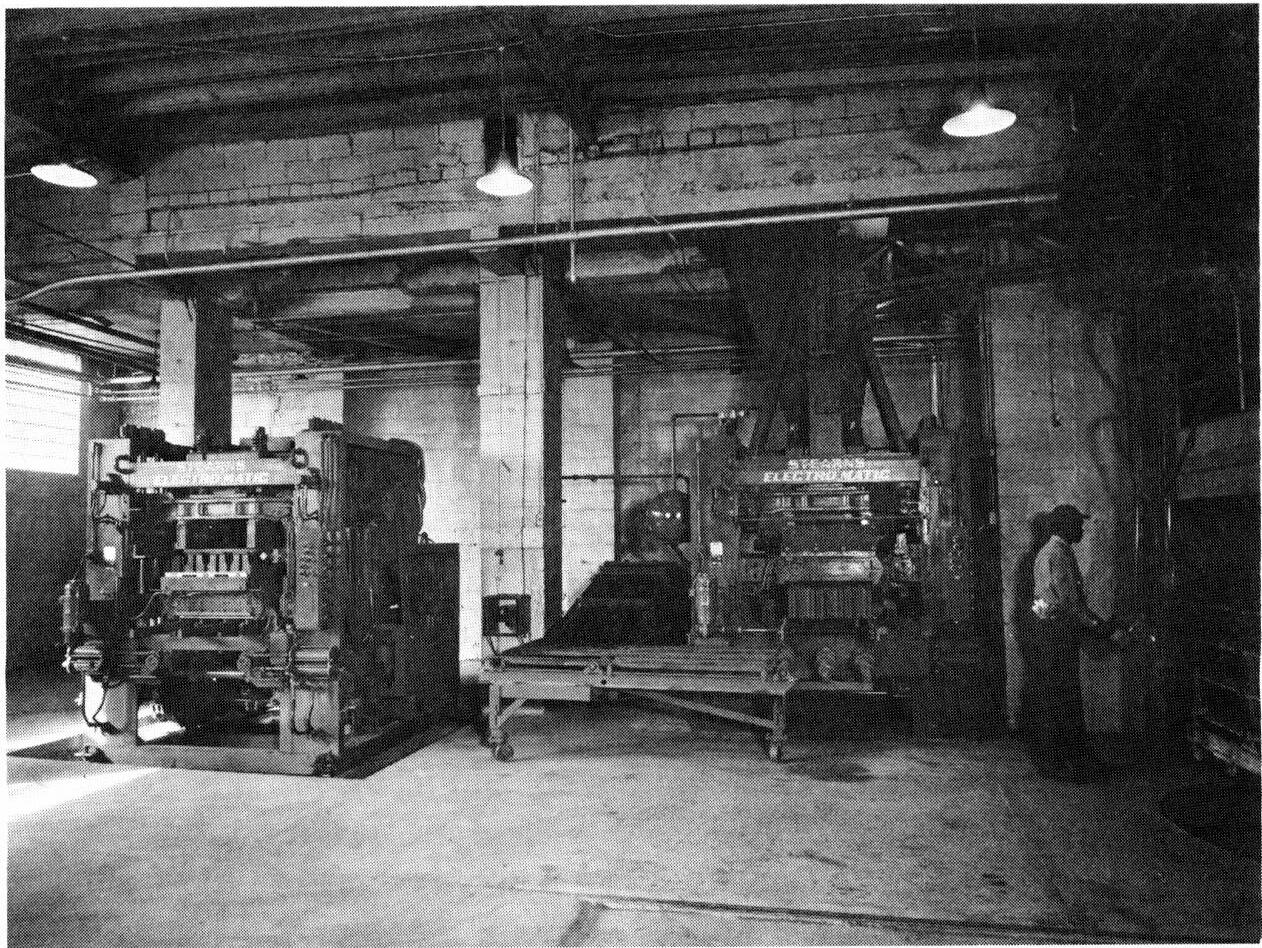
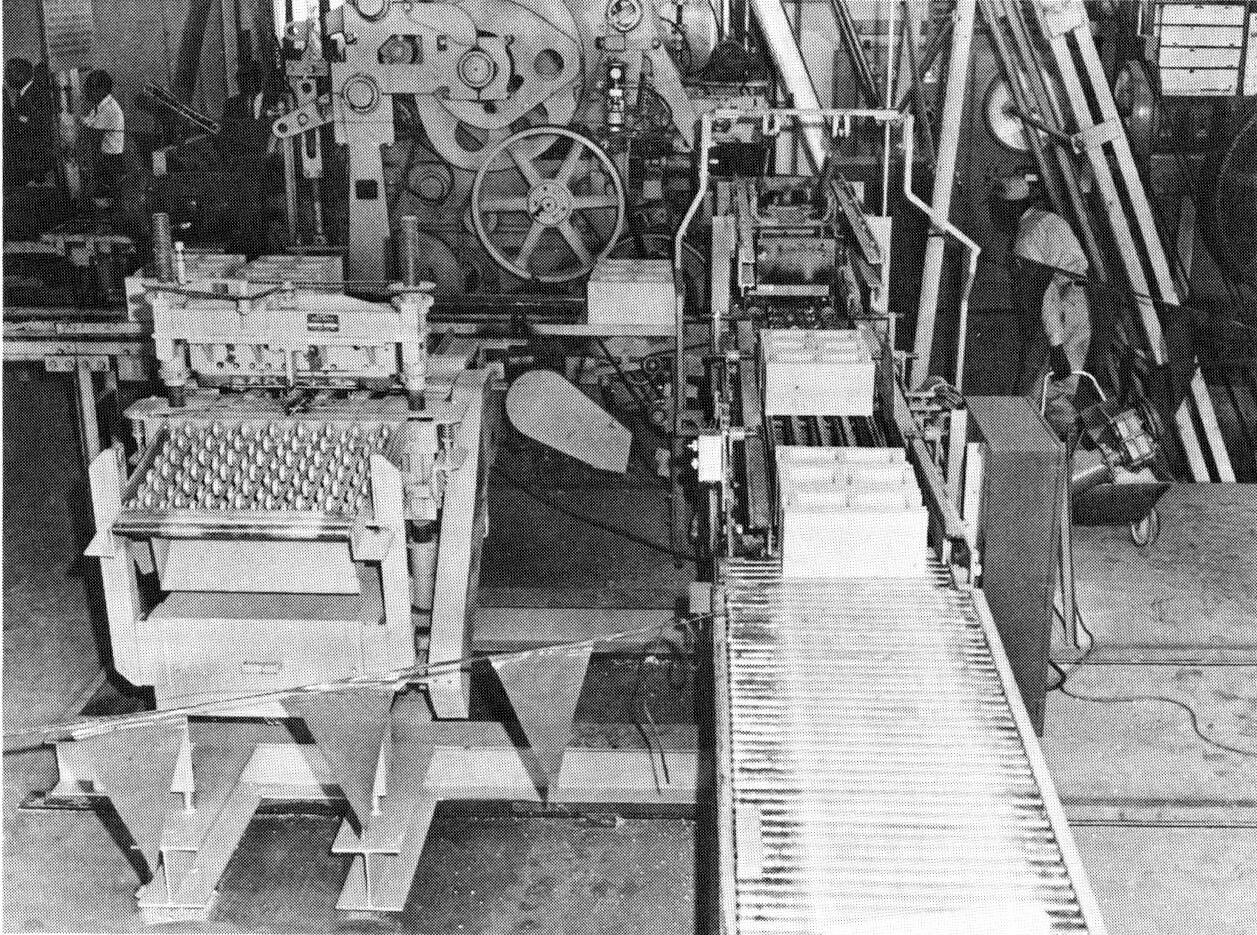
135
Another pair of modern, high speed block machines.
This photo shows a Besser high speed block splitter and a block turnover. The block plant has reached the age of automation.
Development of Specifications for the Concrete Block Industry
By Benjamin Wilk
The evolution of the concrete block industry has been greatly influenced by the specifications governing its product particularly those adopted by the American Society for Testing Materials (ASTM), whose specifications are generally used by architects and engineers.
The last 60 years of product evolution have seen a parallel development of specifications for concrete block, designed always to protect both the user and manufacturer. There is, however, a profound difference in the way the changes have taken place. Where the modifications and improvements in product were steady and constant, the ASTM specifications for concrete block remained practically unchanged for some 35 years prior to 1966. The basic block specification was proposed as tentative in 1931, and with slight revisions became standard in 1936. There were further minor revisions in 1939, 1944, 1952 and 1959, but the first major revision in the code didn't occur until 1966.
The earliest specification for hollow concrete block was proposed by the National Association of Cement Users in January, 1908. (The NACU was organized in 1904 and continued under that name until 1913 when it became known as the American Concrete Institute.) In 1905, the United States government adopted concrete block for its hospitals, warehouses and barracks in the Panama Canal Zone and the Philippine Islands. Before taking this step, the government subjected the product to thorough and rigid tests. In the same year, a committee headed aptly enough by a man named O. U. Miracle was appointed to formu late the first national specification for concrete masonry units, and its recommendations were presented three years later.
The 1908 specification called for the block in bearing walls to have an average strength of 1,000 pounds per square inch or 28 days with a minimum of 700 pounds per square inch. Air space was limited to 33% and absorption was to average not more than 15% (with no single block to exceed 22%). Absorption was to be measured on a block placed in a pan of water at least 2" deep, and had to pass a ¼" mesh sieve; stone or clean-screened gravel was to go through a ¾" sieve and be refused on a ¼" sieve. A 1-3-4 semi-wet mix was recommended for exposed bearing walls, and a 1-3-5 mix for a wet cast block. Portland cement mortar was recommended.
136 XV
Tranverse, compressive and absorption tests were required, along with freezing and fire tests when necessary, and the modulus of rupture at 28 days was to average 150. Any expense attending such tests was to be met by the manufacturer of the block.
This first standard specification was adopted in 1910. Two years later, the practice for curing which until that time had consisted of sprinkling with water for seven days was revised slightly by the addition of a new method: the use of steam from 100° to 130° for 48 hours with a subsequent storing of eight days. This recommended practice was the first mention of high pressure steam curing in block specifications.
Also in the proceedings for 1912, Robert Havlik who later became active in the construction of concrete block buildings at Moosehart, Illinois suggested the use of high pressure steam curing similar to that used in curing sand-lime products. He predicted that in the future all concrete products would be cured in this way, mainly because this method would make them ready for the market within 48 hours. He went so far as to say: "No concrete products manufacturer should cure by sprinkling unless he cannot afford steam curing."
Havlik, unfortunately, was years ahead of his time. Lack of interest in this form of curing for more than a decade after Havlik first suggested it was apparently due to the comparatively high cost of equipment in relation to production. But a large proportion of concrete products manufacturers eventually took Havlik's advice and are now using high pressure steam curing.
In 1916, the absorption rate was changed to 10 per cent at the end of 48 hours. In 1922 came the first specification for a non-load bearing unit, with a requirement of 300 pounds per square inch. That same year, the following table of strengths was suggested:
Heavy load bearing: 1,200 psi (allowable load 200 psi)
Medium load bearing: 700 psi (allowable load 75 psi)
Light load bearing: 500 psi (allowable load 40 psi)
Non-load bearing: 250 psi
The American Concrete Institute accepted this table as tentative in 1923. The absorption time, however, was shortened from 48 to 24 hours. A similar table with the elimination of the light load bearing unit was accepted as tentative in 1924, and adopted the following year.
In 1928, the heavy load bearing classification was eliminated and a paragraph inserted stating: "where unusually heavy loads are to be carried the average strength should be ten times the figured super-imposed load." The phrase "non-load bearing" was revised to read "sufficient strength to be handled." (The strengths mentioned were 28-day strengths).
137
This was the last standard specification with the official sanction of the ACI. In 1930, this organization turned the preparation of standard specifications for concrete masonry units over to the American Society for Testing Materials. In the meantime, a 700 lb. strength requirement was adopted by the ACI as the minimum strength of units for load bearing walls eligible for fire retardant ratings.
In 1931, the ASTM adopted tentative specifications for hollow concrete masonry units. They were revised in 1933 and 1934 and adopted as standard in 1936. The 1936 specifications prescribed that at the time of delivery to the job, the units should conform to the physical requirements given in Figure 95.
Also in 1931, the Federal Specifications Board approved specifications for hollow concrete masonry units for the use of the departments and independent establishments of the United States Government in the purchase of this product. These specifications were the same as those approved by the ASTM, except that in the absorption test, only three samples had to be tested instead of five and absorption could not exceed 16 pounds per cubic foot of concrete instead of the 15 pounds specified by ASTM.
The Federal specifications were also the first to eliminate the age requirement of 28 to 30 days before testing or delivery (first proposed in 1907) and to limit the moisture content to 40% of the total absorption. This last provision was made in an effort to eliminate the delivery of wet, green block to the job.
The 10 per cent water absorption requirement of 1916 had been based on a concrete block weighing 140pounds-per-cubic-foot of concrete. This was the forerunner of the 15-pound-per-cubic-foot water absorption in the ASTM specifications. There was no reference to maximum moisture content in the old American Concrete Institute specifications, and even though the ASTM set the moisture content limit at 40% of total absorption at time of delivery, this requirement was rarely enforced in the immediate years after its adoption.
This situation changed, however, after the end of World War II. At this time, there was an unusually big demand for block, and some manufacturers were delivering improperly cured or "green units." Many users, particularly the Corps of Engineers, were dissatisfied because of the excessive cracking of walls built with the green block. The immediate result was sudden enforcement of the restrictions on both absorption and moisture content.
The Corps of Engineers was still dissatisfied with the 40 percent moisture content requirement and adopted a suggestion by Carl Menzel of the Portland Cement Association that block meet a relative humidity requirement, instead, measured on an apparatus developed by Menzel. At the same time, the ASTM studied the Menzel suggestion and adopted it as tentative. It never became standard, however, because various subsequent investigations indicated extreme difficulty in producing test results in the average laboratory. The Corps of Engineers finally went back to a moisture content of less than 40 percent.
138
As a part of continuing efforts to improve the quality of block, the National Concrete Masonry Association, through its technical committee and its sub-committee on codes and specifications, spent a number of years trying to come up with a specification that would satisfy all manufacturers. The problems involved in coming up with one specification right for all fifty states with their varying climactic conditions, ranging from the very dry to the very wet, and with manufacturers using widely different curing methods and aggregates were almost insuperable. After seven drafts, however, the NCMA submitted a suggested specification which the ASTM adopted as tentative in 1966. It materially changed the standards that had been in use for many years.
Product manufacturers using high pressure steam curing felt that this system produced a block with less volume change than the units produced with high temperature or atmospheric curing. To support this view, they began making comparative tests, and to standardize testing methods, the NCMA made a detailed study of the reference, the rapid and British methods of determining volume change or linear shrinkage. From the standpoint of reproducibility in the laboratory and time involved, a modified British method was deemed best. Accordingly, a linear shrinkage factor was developed which was combined with moisture content into a table that could be used in three relative humidity conditions virtually covering the fifty states. (See Figure 96.)
Three grades of block were listed to be used under various conditions governed by strength, water absorption and moisture content. Provision also was made for moisture control and non-moisture controlled units, (See Figure 97) and a new idea was introducedby specifying minimum face shell and web thicknesses.
As soon as the concrete block industry had time to reflect on the 1966 specifications, there were complaints that they were too complicated. Manufacturers felt that three grades of block were too many and that architects and engineers would ask for the top grade even though the lower grades would be perfectly acceptable for the job at hand. As a result of the many complaints, a task force of Sub-Committee III of Committee C15, ASTM, was appointed with S. H. Westby as Chairman to see if a more suitable specification could be developed.
After several drafts, the task force has come up with a modified specification which, at this writing, appears acceptable to the ASTM. The major change from the 1966 specification is the elimination of one grade of block, and the provision for a special lightweight block weighing less than 85 pounds per cubic foot of concrete. (See Figure 98) The minimum thickness of face shell and webs remains the same as that in the 1966 tentative specifications. (Figure 99)
Specifications are the result of man's attempt to reach agreement on acceptance of criteria for a product. It is just as difficult in 1969 to formulate concrete block specifications that will please everyone involved as it was in 1966 or 1939. Over the years, however, the efforts in this direction have always been toward growing use of a dependable, high quality product. To the degree that the industry has moved toward this goal, the aims of the men who have
139
helped create concrete masonry specifications have been realized, and it is hoped that the specifications under consideration in 1969 as well as those that will be considered in the future will be evaluated in that light.
Figure #95
Physical Requirements of Hollow Load-Bearing Concrete Masonry Units American Society for Testing Materials Standards– 1936
Compressive Strength, Minimum per square inch (Average Gross Area) Water Absorption, maximum lbs. per cu. ft. Moisture content, maximum per cent Minimum Face Shell Thickness, in inches
Average of five Units Individual Units Average of five Units Average of five Units 700 600 15 40 1 ½“ or over Under 1 ¼“ and over ¼ “ 1,000 800 15 40
Figure#96 MOISTURE-CONTENT
REQUIREMENTS
FOR TYPE I UNITS. Moisture Content, Maximum, per cent of Total (Average of 3 Units) Humidity* Conditions at Job Site or Point of Use
Linear Shrinkage, per cent Humid Intermediate Arid 0.03 or less ............. 45 40 35 From o.03 to 0.045 ....... 40 35 30 0.045 to 0.065 (Max.) .... 35 30 25 * Arid -Average annual relative humidity less than 50%. Intermediate -Average annual relative humidity 50 - 75%. Humid -Average annual relative humidity above 75%.
Figure#97
STRENGTH AND ABSORPTION REQUIREMENTS.
Compressive Strength, min. psi Water Absorption, max, lb/ft3 (Average of 5 Units) Average Gross Area Average Net Area Oven-Dry Weight of Concrete, lb/ft3 Gradea Average of 5 Units Individual Units Average of 5 Units Individual Units 125.1 or more 120.0 to 125.0 115.1 to 120.0 110.1 to 115.0 105.1 to 110.0
105.0 or less U-I, U-II......... 1,000 800 2,000 1,600 10 11 12 13 14 15 P-I, P-II ......... 1,000 800 13 14 15 16 17 18 G-I, G-II......... 700 600
140
Figure #99
-MINIMUM THICKNESS OF FACE SHELL AND WEBS.
Web Thickness (WT)
Nominal Width (W) of Units, in.
Face-Shell Thickness (FST ), min, in a Webs, a min, in.
Equivalent Web Thickness, min, in./ lineal ft b 3and 4..... ¾ ¾ 1? 6........... 1 1 2¼ 8........... 1¼ 1 2¼ 10.......... 1? (1¼) c 1? 2? 12........... 1½ (1¼)c 1? 2?
a Average of measurements on 5 units taken at the thinnest point, when measured as described in Methods C 140, Sections 14 and 16(6).
b Sum of measured thickness of all webs in unit, times 12, divided by length of unit.
c Face-shell thickness (FST) shown in parentheses is applicable where allowable design load is reduced in proportion to the reduction in thickness from basic face-shell thicknessesshown.
STRENGTH AND ABSORPTION REQUIREMENTS
Compressive Strength minimum, psi Water Absorption, max., lb/CF (Average of 3 Units) with Oven-Dry Weight of Concrete, lb/CF Average Gross Area Weight Classification Grade
Special Lightweight Less Than 85
Average of 3 Units Individual Unit
Lightweight Less Than 105
Medium Weight Less Than 125 to 105
Normal Weight 125 or more G-I G-II 1,000 800 18 18 15 13 S-I* S-II* 700 600 20
NOTE: To prevent water penetration protective coatings should be applied on the exterior face of basement walls and when required on the face of exterior walls above grade.
* Limited to use above grade in exterior walls with weather-protective coatings and in walls not exposed to the weather.
141
Figure #98
GalleryofModernConcreteMasonry
Buildings
Today, the early visions of the pioneering architects and builders who saw great esthetic as well as structural qualities in concrete block are being realized. All over North America, beautiful structures of concrete block are reaching for the sky, where once they were most often hidden beneath the ground.
Even so, the possibilities of concrete block have only been scratched. The pictures of modern concrete block structures plus a wide variety of other current uses of block on the following pages are not an end but rather a direction. They are signposts pointing to the future of concrete block, a future limited only by the vision of the people who make it and build with it.
XVI
143
XVII But Not Endings . .
What's ahead?
Where does the 50-year-old NCMA and the 75-year-old domestic concrete block industry go from here? After 1970 . . . . what?
Of course, any answers to this question must be speculative. But the signposts are abundant and they seem to be pointing in some rather specific directions.
What are some of these directions?
There seems little question that the trend toward merger and consolidation of the concrete block industry into fewer and larger producers will not only continue but will probably accelerate. Thus the "backyard" industry will come half-cycle and lock there. An industry of small, often unsophisticated, frequently inefficient individualists will soon be an industry of large, automated producers steeped in modern business philosophies and techniques.
Present indications of this trend are irresistible. In one recent day, the number of block producers in Milwaukee, for example, was cut in half by merger. Clay brick companies are now getting into the block business in growing numbers, and some block industry leaders feel that by the turn of the 21st century, there may be no clay brick business as we know it in 1969. "It's like TV and the movies," said one. "The brick people are no longer trying to lick us; they're just joining up."
Within a decade, there will probably be half as many companies making block in the United States as there are today. Some industry leaders would cut even that figure in half. This kind of consolidation will mitigate and perhaps eliminate some of the more irritating problems with which the industry has lived all its life. Probably the best example is price-cutting. The increasing management sophistication that will come with consolidation will probably eliminate many of the suicidal aspects of price wars. There will still be competitive pricing but not at the sacrifice of profits. Cost accounting will be more exact and price competition will be on the basis of effective management. This will tend to eliminate the weak and ineffective producers but it will no longer ruin the market for the efficient producers as well.
144
The fewer, larger block producers will offer much more customer service than they ever have before. After more than a half-century of industry operation, many block producers still tend to make the block, store it in their yards, and wait for someone to come around and buy it. This throwback to the Neanderthal period of the industry is slowly being replaced by the concept of customer service and this concept will almost surely grow in the years ahead, probably in three primary directions: the producer will build entire wall sections in his plant; he will send block experts into the field to build walls on the job site; or he will build the entire job himself. Only in this way can he control the quality of the end product and make full use of this own expertise in the use of his block.
All plants will be fully automated to cut labor costs (and problems) and turn out a better, more uniform product. There will be faster runs and more consistent quality. Automated equipment will be capable of turning out everything from individual block to entire wall panels meeting rigid specifications, ready for delivery to the job site and instant placement in the structure. Those producers who are unable to automate will be left by the wayside; they will have to be able to compete in the world as it is and for the block industry, it will surely be a world of automation.
Plants will be much larger, representing greater capital investment. There will be fewer plant workers in relation to total production. There will probably be regional and perhaps even national ownership of block plants. There may even be chain block makers like Howard Johnson's or Kroger's in which customers can have absolute confidence of consistency of quality and design in the product.
Since builders are also becoming national organizations, we may one day soon see huge construction corporations buying from national suppliers of concrete block. Thus regional or national contracts by block producers with builders will make single orders of block in the millions almost commonplace.
Since the industry has already come up to a point of acceptable technology in its ability to produce consistent quality, the technological emphasis in years ahead will be more on imp rovements or refinements than advancements. Automation will be carried to its ultimate conclusion a push button plant. Block will eventually be conveyed automatically to the curing chamber, then to a machine for panelization of whatever size needed, with windows, doors and a finished surface texture added automatically. But the first refinement in block production will probably be higher speed machines and those producers who don't want to be gunned down had better get behind the machines or get out of the way.
An increasing share of this exploding, automated, high quality production will be going into multi-storied buildings presently the most promising star in the marketing firmament of concrete block. Right now, block can go to 20 stories. Very soon it will go twice, three times that high. All that is needed is to increase the strength of the units. Today they are standard at 1,000 psi. For a 20-story building, they must be 3,000
145
and for a 40-story building, 7,500 psi. They can be made strong enough now, but the costs are too much higher.
These problems are being resolved, and when they are, block will reach higher and higher for the sky. Block is considerably less expensive now than competitive materials in high rise construction. But the total cost of construction with block remains high so it is essential that other necessary services be integrated into the block walls at low cost. This is being explored, and when it is accomplished, the possibilities in block will be almost limitless in multi-story construction where repetitive sizes are required.
This promise will be realized when the industry accepts the premise that the concrete masonry unit must ultimately serve all the functions that a wall requires. This means an acceptable or better yet, highly attractive outside appearance, maintenance free exterior, built-in insulation, and structural capabilities that block presently lacks. There will be prefabricated utilities within the block and new developments in mortar that will make the block wall an integral unit. There will be a more precise, uniform unit, with closer tolerances both for interlocking systems and standard units. And there will be progress toward securing a very fast set so the block will hold its tolerances precisely through the curing period.
The block producer today is entirely dependent on others for his livelihood. Dozens of worthwhile construction techniques have been evolved for block that never really caught on because the block producers had to depend on others to carry them forward. This will change with the growing concept of integrated walls. Building with individual units will give way in a growing number of construction projects first to building a wall on the job site, then to building a wall at the factory and taking it to the job. There will thus be none of the vagaries of onsite labor to contend with. There will be complete control by the block producer of the performance of the wall, because he has supervised its construction in his own plant.
The Battelle Institute is presently looking into methods by which the block industry can automate wall construction. With such information the industry will evolve complete systems for this purpose and the production and delivery of finished block walls with fully integrated services will become the norm.
Not all of the growth, however, will be in this direction. Many types of construction that will be coming on strong in the decades ahead offer potent possibilities for more conventional block construction. There is growing acceptance of block, for example, in multi-family dwellings; new and exciting configurations of block will become profitable with massive sales to this market. Meanwhile single family homes presently priced out of mass markets will come back to favor with concrete block units that are easier and faster to lay up in a wall because of new and better adhesives and mortars.
146
This market will also stimulate the growth of interlocking block systems, and there will be more combined development and promotion of these systems by groups of companies, merged into a marketing chain for this purpose. Exotic epoxies applied from a caulking gun may replace mortar and trowel. And there will be much more efficient use of new products in water-proofing materials, plastics, and insulation in combination with concrete block.
Competition will take a new direction. Materials with insufficient construction volume to sustain them on a mass basis now new plastics and metals, for example will be the wave of the construction future, and block makers will have to learn to live with them. They may very likely be competitive on in-place cost if not in material cost very soon. So the block industry will need to sophisticate its technical knowledge to cut in-place cost of block construction again probably through the factory production of integrated walls.
The block industry is still, to a large extent, run by patriarchs who have engineered its evolution over the past five decades. Their primary interest and primary thrust has always been in making block. Make the best possible block, they reasoned, and everything else will take care of itself. This is no longer true. Very soon they will have the perfect block, mass produced with high consistency. The major problem then becomes finding someone to buy it. As one relative newcomer to the industry pointed out: "Intellectually they understand this, but deep down in their soul they hate the idea because they still get their greatest pleasure from making the block."
Pleasure or not, this emphasis will have to change in the years ahead. So will a lot of other habits. The old-timers who persist in looking to contractors and builders, for example, as their primary customers, must begin to look in other directions. The money people make the decisions, now, and the leaders of the block industry must find who they are, how they decide and then convince them of the advantages of concrete block. These people will be the big block customers in an automated, mass-produced, high rise, big money construction society in the years ahead.
Obviously, a trade association designed to deal with such drastically changing conditions and an industry in transition is going to have to change, too both in philosophy and operation. It will have to reflect the new marketing rather than manufacturing orientation of the industry, and it will have to offer new services in keeping with the modified nature of an industry made up of fewer, larger companies. As this trend becomes more pronounced, Associations of similar building products might quite likely merge to provide a coordinated attack on common problems. A Unit Masonry Association, for example, might well be a logical future development. State associations will probably have to broaden their approach first, dealing with problems peculiar to the area for a growing group of building products manufacturers. Eventually, this breadth of product approach may invade the national Association picture, as well. There may also be a merger of associations vertically portland cement, ready mixed concrete and concrete
147
masonry, for example. These industries are already moving in such a direction in some states, and there is no reason to suppose that the trade associations serving them won't do likewise.
There is by no means unanimity among those closest to the concrete block industry today on what the future holds in store. Listen, for example, to several industry leaders musing on this question some who have grown up with the industry, others who have brought fresh blood to it from the vantage point of youth or other business orientations:
"The future of the block business is endless. The rebuilding of the cities and the expansion of population, these are our markets. And one day we'll get the house foundation business back too;"
"Block is going to grow and grow in exterior walls of homes where it can be seen because it is going to get steadily more attractive;"
"There are going to be ever more important uses of block in buildings stories without eaves or copings. But overall design and workmanship is vital in this growth; we dare not put the growth of block in the hands of inexperienced and uncommitted men;"
"With the demand for high-rise and the need for rehabilitating the blighted areas and the explosion of population, the demand for block all over the country will be in the billions;"
"Ten years from now there will be no racks, no lift trucks. Cement will be pre-shrunk and pre-set, block will be delivered to the job the day after it is made in panelized units, to be erected by block laying machines. The mason of tomorrow may lay 6,000 block a day, and mortar may be obsolete because of interlocking block systems, faced to make the block resemble anything the builder desires;"
"Fifteen years ago, three-fourths of the cooperative effort in the industry was directed at manufacturing problems. In the next decade that figure will be reversed. Technical promotion will be the order of the day and the promise of the future;"
And, finally, a thought for all ages, from a block industry pioneer: "To grow further, this industry will continue to need the ideals, the will, the know-how and the critical cooperation of the architect who too often lets the contractor use the cheapest material he can find."
This, then, is the face of an industry in transition an industry with a virtually unlimited future. According to the F. W. Dodge Construction Market Outlook, housing still the basic market for concrete block will
148
come out of the doldrums of the late 1960's and turn into a booming construction market in the 70's and 80's. This resurgence of housing construction plus greatly expanded public building virtually insures burgeoning markets for the block industry in the immediate years ahead.
This is both an opportunity and a challenge. The housing demand is expected to grow at a 5.4 per cent annual rate through 1980, with public facilities attaining almost the same percentage of growth. Although business and institutional gains will be much more modest, an overall annual construction growth rate of about 4.3 per cent is projected for the next decade. This is the opportunity. The challenge is to change old concepts and techniques in some of the ways described earlier to take maximum advantage of these manifold opportunities.
The NCMA's executive director, Paul Lenchuk, put it this way: "What the block industry needs is a change of attitude. We have got to start believing the fact that we have the finest building product with the greatest potential."
When that happens, and when it comes together with new technology and burgeoning opportunities, concrete block will be on its way to a growth limited only by the vision of the men who are working within this industry on the 50th anniversary of the trade association it spawned. There were more than 3 billion 8" x 8" x 16" equivalent units of block sold in 1969. That's a lot more than the several hundred thousand sold 50 years ago. But it will pale in comparison to the billions sold at the end of the next 50 years.
149