VOLUME 13 | NO 5 SEPT/OCT 2026
INDUSTRIAL THE OFFICIAL JOURNAL OF THE AUSTRALIAN INSTITUTE FOR NON-DESTRUCTIVE TESTING
RADIOGRAPHY
ULTRASONICS
VIBRATION ANALYSIS
EDDY CURRENT
LUBRICATION ANALYSIS
PENETRANT
THERMOGRAPHY
EYE
MAGNETIC PARTICLE ACOUSTIC EMISSION
CORROSION INSPECTION STARTS WITH US.
Krautkrämer PAXYS: Less Than 1 kg. Full Phased Array Performance. Built on 75+ years of ultrasonic innovation, our new Krautkrämer PAXYS brings fast and reliable corrosion mapping to challenging oil & gas environments. It produces encoded C-scan thickness data without proprietary hardware or compromising on data quality – all at the hands of a single inspector. Powering it all is comPAct, our patented, thumbsized chip with full phased array capability inside. Scan the QR Code to learn more! Or visit our website at waygate-tech/paxys
AINDT NEWS
AINDT NEWS
President's Message Pick up a careers guide at any high school and look for NDT. You won't find it. Electrician, plumber, fitter, they're all there. Our industry, which keeps pipelines, bridges, aircraft, and power stations safe, barely gets a mention. For those who do find NDT, the first year is the hardest. Certification needs experience hours, and experience needs someone willing to take you on before you're certified. That is a real cost for employers. A trainee isn't billable for a while, and on a tight contract, that is a hard thing to justify. So a lot of businesses wait for someone else to train people, then hire them once they have their tickets. When everyone does that, the pool shrinks. The upcoming workforce study will give us a clearer picture of where the gaps are, but you don't need a study to see that the entry point is where we lose people. Some never hear about the industry. Others get a foot in the door but can't find a way through to their first certificate.
That is where AINDT has a role. We sit right in the middle of the employers, the training providers, and the certification scheme. Sam Hallifax
A young person who has never heard of NDT can't choose it. The ones who do end up with us usually get here through a side door, and we lose a lot of good people who never find that door at all.
I know this firsthand. I was waiting to go back to uni when a traineeship came up, and I applied more or less on a whim. Geoff Ackerman and Eric Kreutzer took a chance on me. I had no background in NDT and no real idea what the job involved, but they gave me a go anyway and partnered me with good teachers. Angus Burnett taught me radiography, and a lot of what he showed me I still think about today.
The pay, the travel, and the work stack up well against most trades. The problem is that almost nobody outside the industry knows that.
Industrial Eye September/October 2026
We are well placed to make the pathway easier to see and easier to follow. It is a conversation I want to have with the Federal Council and the branches, as well as with the businesses who are already taking trainees on and making it work. Some of our members are doing this well already. They have built their own trainee programs or brought people across from other trades. It would be good to hear more about what's working, and I would like to share it. On the international side, the MoU work with BINDT and NZNDTA continues. For anyone starting out, knowing their certification can travel with them is a strong reason to stay in the industry. Someone took a chance on me once. We need more people in a position to do the same, and a clearer path for the ones coming through. Sam Hallifax President, AINDT Global SME & Business Improvement Manager, EnerMech
3
CONTENTS
11
14
AINDT NDT News News
Technical Articles
CEO Message Member List An NDT Update Certification from the Board Membership Update Registrar NDT Condition Certification Monitoring Board Training UpdateCentres Condition AuthorisedMonitoring Qualifying Training Bodies Centres Authorised QueenslandQualifying Wales Branch Bodies Update Queensland South Australia Wales Branch Branch Update Update South Victoria Australia Branch Update Branch Update Victoria Western Branch Australia Update Branch Update Western Australia Branch Update
6 9 10 12 14 13 15 18 18 19 19 20 20 22 23
Thermography in Action Standards Update Northrop Grumman: A Great Career Choice Thermography in Action NDT World Event Calendar Northrop Grumman: A Great Career Choice NDT World Event Calendar
11 14 11 24 16 46 24 49
Industry News Industry News Standards Update
FEDERAL EXECUTIVE OFFICERS
VICTORIAN BRANCH
SOUTH AUSTRALIAN BRANCH
President: Mr Sam Hallifax Immediate Past President: Mr Joshua Morris Vice President: Mr Ian Hogarth Treasurer: Mr Damien Clarke Secretariat Liaison: Mr Peter Milligan CEO: Mr Stuart Norman
President Mr Amir Katouzi Past President Mr Paul Trigg Vice President Mr Peter Milligan Treasurer Mr Samad Asghary Secretary Mr Glen Haberl Official Address PO Box 52 Parkville VIC 3052
President Mr Andrew Morris Past President Tyson Jenke Vice President Mr Luke Jones Treasurer Mr Matthew Hobbs Secretary Mr Nicholas Hart Official Address PO Box 538 Kent Town DC SA 5071
QUEENSLAND BRANCH
WEST AUSTRALIAN BRANCH
President Mr Steven Kennedy Past President Mr Jim Tibani Vice President Mr Dean Terry Treasurer Shaina Johnson Honorary Secretary Mr Roger Hardy Official Address PO Box 301 Cleveland QLD 4163
President Mr Nathan Lenane Past President Mr Joshua Wilkinson Vice President Mr Nicholas Chortis Treasurer Mr Michael Needham Secretary Mr Paul Lavender Official Address Level 7, 256 Adelaide Terrace Perth WA 6000
NEW SOUTH WALES BRANCH President Mr Frank Galea Vice President Mr Neil Burleigh Treasurer Mr Paul Ashby Secretary Mr Matthew Thompson Official Address 45 Jenkins Street Douglas Park NSW 2569
4
Reflections on NDT Personnel Certification in Australia Is it Time to Include Human Factors Education for NDT Technicians? Power of Process Control in Software Driven NDT Procedures Impedance Spectroscopy of B40 Concrete During Hydration for Non-Destructive Strength Prediction A New Methodology to Predict Moisture-Induced Stiffness Degradation in Bio-based Composite Sandwich Structures using Acoustic Emission Wave Velocity
26 28 32 31 36 35 41 39
Industrial Eye September/October 2026
CONTENTS
31 Products & Services Condition Monitoring Group OMS Russel Fraser Sales SmartChem Industries SRG Global Total Asset Solutions
47 47 47 48 48 48
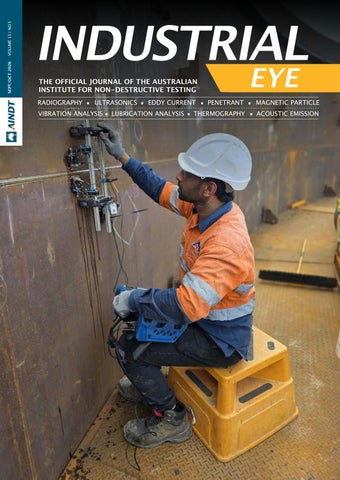
Cover photo: Time-of-Flight Diffraction (TOFD) inspection of a horizontal shell-to-shell weld on a storage tank. Photo supplied by Sooraj Uttumadathil Subramanian, ARL Laboratory Services.
Production Sally Wood Design Alarna O’Connell AINDT PO Box 52, Parkville Vic 3052 P: (03) 9486 9267 www.aindt.com.au E: federaloffice@aindt.com.au ADVERTISING AINDT Federal Office P: (03) 9486 9267 E: sally@wordly.com.au
Industrial Eye September/October 2026
INSTRUCTIONS TO AUTHORS OF TECHNICAL ARTICLES Manuscripts should be submitted in electronic form: 1. in word 2. typed with single spacing 3. with figures as tif or jpeg files at better than 300dpi
Manuscripts should include: 1. symbols and abbreviations conforming to recognised standards; metric units (SI) 2. references listed, after the text, in the order in which they occur in the paper 3. references indicated in the text by arabic numerals in square brackets 4. tables and figures numbered separately but consecutively with Arabic numerals and brief, descriptive titles
5. a reference in the text to all tables and figures 6. graphs and diagrams made with lines of sufficient thickness to reproduce well 7. titles and address of authors Procedure for submission of manuscripts: 1. articles should be sent to: journal@aindt.com.au 2. manuscripts will be submitted to referees who will remain anonymous 3. reprints of each paper will be supplied free to the author Published by: The Australian Institute for Non-Destructive Testing, PO Box 52, Parkville, Vic 3052 Australia ISSN: 2203-2940
5
AINDT NEWS
A Message from the CEO As we move into the final quarter of 2026, I want to begin by thanking the volunteers who give so much to the AINDT. Their contribution is felt throughout the Institute, often through work that happens quietly behind the scenes, alongside demanding jobs and family commitments. I particularly want to acknowledge Paul Grosser, who has been acting Certification Services Manager while we have been searching for someone to take on the role. Paul has given an enormous amount of time and energy to helping us maintain this essential service. His willingness to step in, share his knowledge Stuart Norman and support the office through this period has been greatly appreciated. It has been an almighty effort, and I am personally grateful for the commitment he has shown to the AINDT and our certification holders. My sincere thanks also go to all outgoing Branch Councillors, including our Branch Presidents (Josh Wilkinson in Western Australia and Tyson Jenke in South Australia) and other office bearers. Organising branch activities, supporting members and keeping local networks connected takes considerable effort. These responsibilities are frequently carried out after hours, and the time involved can easily go unrecognised. Your service has made a real difference.
I would also like to thank the employers who support their staff’s involvement in the AINDT. Their support is greatly appreciated and makes an important contribution to the Institute and the wider NDT community. Across our branches, Certification Boards and committees, volunteers provide the expertise and practical support that allow the Institute to function. The AINDT simply could not operate without this extensive network of people willing to contribute. To everyone who has served, and those continuing or stepping into a role, thank you. I am incredibly grateful.
6
Opportunities for Our Industry
Looking beyond the Institute, gas development in Australia presents potential opportunities for our industry. The Beetaloo Basin in the Northern Territory is a significant example, with development involving gas production and processing infrastructure, alongside proposals for pipelines to connect supply with markets. The scale of the infrastructure contemplated highlights the importance of planning for the skills and services needed to build and maintain it. For NDT and condition monitoring professionals, I see potential demand extending from fabrication and construction through to commissioning and ongoing operation. Inspection and monitoring of operating plant depend on competent people applying appropriate methods. As projects progress, our industry has an important contribution to make to their safe and reliable operation. We should be thinking now about how we prepare people for that work. Employers, training providers and experienced practitioners all have a part in developing the next generation of technicians. Maintaining current certification and building relevant experience will help our workforce respond as opportunities emerge.
AINDT Certification
That brings me to a practical reminder for everyone holding AINDT certification. You can apply to renew or recertify up to six months before your certification expires. Please make use of that window. Check your expiry dates, understand which pathway applies to you and begin gathering the necessary evidence well before your application is due. We are currently processing complete applications in under 10 days. However, that turnaround depends on receiving all required information. Missing evidence, incomplete forms or outstanding signatures can delay an assessment. Where examinations are required, candidates also need to allow time to arrange and complete them. Leaving everything until the final days creates pressure that is usually avoidable.
Applying early gives you time to resolve questions and helps avoid late or expedite fees. It also reduces the risk of a lapse in certification affecting your work.
Industrial Eye September/October 2026
AINDT NEWS
candidates and the office. For now, please download the current forms, complete all relevant sections and upload them with your application. Check that signatures are present, attachments are legible and the required evidence is included.
Please treat renewal and recertification as something to plan for, particularly around busy work periods, travel and leave.
I also want to explain why completing the required forms and uploading them to the portal remains an essential part of applying. These forms help us collect consistent, verifiable evidence and meet the requirements of ISO 9712:2021. They support proper assessment of each application and help maintain confidence in the certification that our industry relies upon.
I encourage candidates to start preparing early and contact the office if they have any questions about what is required. Our team is happy to provide guidance so you can gather the necessary documentation and submit a complete application that we can process promptly.
The downloadable format offers candidates useful flexibility. You can download the relevant forms, complete them outside the portal, gather supporting records and obtain the necessary signatures from appropriate referees before submitting your application. This allows you to work through the requirements with the people who need to verify your information, rather than trying to organise everything during submission. We are considering how best to develop the portal into the future, including how it can better support
Finally, I was deeply saddened to learn of the tragic passing of Nick Burleigh of EN DE TEK. Nick was the son of Neil, who many within our industry will know. I had many interactions with Nick and always found him helpful and engaging. On behalf of the AINDT, I extend our deepest sympathies to Neil and his family, and to Nick’s friends and colleagues during this difficult time. Nick will be greatly missed by many across the NDT industry. Stuart Norman Chief Executive Officer, AINDT
Krautkrämer PAXYS
Miniaturized technology, Maximum performance
Rethink your corrosion mapping workflow Krautkrämer PAXYS transforms corrosion mapping with fast, reliable phased array inspection in a compact, ultra-portable scanner. It delivers repeatable thickness data, clear C-scan imaging, and efficient single-person operation, helping reduce inspection time and asset downtime. • Ultra-lightweight design, weighing less than 1 kg • X/Y dual-axis encoded scanning for precise, repeatable results • Clear C-scan visualisations for confident corrosion assessment • Ideal for rope access, confined spaces, and challenging field inspections
Official Distributor
Scan for Specs!
Industrial Eye September/October 2026
Proudly supporting Waygate Product users across Australia For more information please email us at
Sales@endetek.com.au
7
eddyfi.com/spyne
AINDT NEWS
Member List October 2026
The AINDT is a national peak body that promotes the professional practices of non-destructive testing and condition monitoring personnel. Our mission is to provide members, industry and the community with independent and professional service in relation to the science and practice of non-destructive testing. Through the work of our state branches and federal office, AINDT is committed to fostering a community of professionals and organisations dedicated to the fields of non-destructive testing, engineering, and materials and quality testing.
We offer a tiered membership structure, inviting businesses to enhance their professional standing and industry influence by becoming a Company, Corporate, or Sustaining member. Our memberships unlock a suite of benefits, including marketing opportunities, heightened support, streamlined staff certification management, and much more. AINDT would like to thank the companies below for their valued support.
SUSTAINING MEMBERS
CORPORATE MEMBERS
ATTAR D R May Inspections EnerMech SRG Industrial Pty Ltd Intertek
Apave Australia Bureau Veritas Australia Core Inspection Services SafeRad SE Asia Pty Ltd
SUPPORTING MEMBERS Chevron Cashcor Engineering
COMPANY MEMBERS NSW
QLD
SA / NT
Bluescope Steel (Port Kembla)
Industrial Mining Inpsection Solutions
SN Integrity
HVT Inspection Services
M-Test Mackay Pty Ltd
AXT Pty Ltd ENDETEK
Monnoo Engineering Services Pty Ltd NBQC and Inspection Services NDT Equipment Sales Pty Ltd Noble Engineering Services Reliance Hexham
Russell Fraser Sales Sci Aps Australia
SmartChem Industries Pty Ltd
International Tube Testing Pty Ltd Queensland Alumina Limited
VIC / TAS ATCL
Gippsland NDT Services Pty Ltd
Global Inspections & Engineering Services Pty Ltd
ASC Pty Ltd
WA
Asset Conformity Testing Services Wood – Asset Performance Optimisation
J & S Castlehow Electricial Services Nexxis Pty Ltd Vertech
NATA
OMS Software Pty Ltd
Thermal Imaging Services (AUS)
Industrial Eye September/October 2026
9
AINDT NEWS
Non-Destructive Testing Certification Board Update We continue to have some terrific turnaround times on applications for renewal of AINDT certification. The best I have seen recently was a 48-hour turnaround on a renewal with the Structured Credit System option. This was a fully complete application with all evidence submitted for the claims in a clear format. Most impressive of all, it was not even an expedited application!
This reinforces a simple message: an application that meets every requirement sails straight through the process. There are no delays, no back-and-forth, and it passes every check the first time. The time to learn how to put together your renewal or recertification application isn't the day before it expires. The best time is right now. The more effort you put into understanding the requirements early, the more smoothly your application will go when the time comes.
Once a certification has expired, you are no longer a certified in that method. All effort will be made by AINDT to give adequate forewarning that a certificate is due to expire. The onus of maintaining certification belongs to the person identified on the certificate. The window for this process opens six months prior to expiry. As we know, the authority to operate is given by the employer, and if a certificate expires, the employer may disallow continued employment. If an operator continues to work with an invalid certificate without informing his employer or client, then all responsibility remains with the operator. If requirements for renewal or recertification are not met on the date of expiry, then the certification shall lapse.
10
If renewal is applied for after expiry and up to 12 months from this date, then a late renewal fee shall apply. If the operator fails to renew after 12 months, then the certificate can only be regained by applying for certification as an initial candidate, including resitting all relevant examinations. If recertification is applied for after expiry and up to 12 months from this date, then a late recertification fee shall apply.
If recertification is applied for more than 12 months after expiry, then it can only be regained by applying for certification as an initial candidate, including resitting all relevant examinations.
Remember, renewal or recertification issued after expiry but before lapsing will commence from the date of approval only, resulting in a certification period that is less than, but not exceeding the 5-year or 10-year total allowed by the standard. Finally, I would like to take the opportunity to announce that the search for a Certification Services Manager has come to an end, with the AINDT selecting a successful applicant. It has been quite some time coming and all members of the Certification Board welcome the news. I would like to thank everyone who applied, particularly those who were unsuccessful. You were all extraordinarily strong candidates in your own right. Further details about the new Certification Services Manager will distributed to members soon. Mark Welland Chair, AINDT NDT Certification Board
Industrial Eye September/October 2026
INDUSTRY NEWS
Standards Update Standards Australia has announced that a new system has been put in place to assist in expediting new and (where required) reviewing old Standards. The new system now has a section of staff from Standards Australian working together with the MT007 Committee to review many ISO Standards.
Therefore, Australian Standards have altered the previous system where a Project Manager was overseeing MT007 and replaced them with a new section. It is expected that having a section of staff will allow for more meetings and faster processing of Standards.
We continue our ballots and work on ISO Standards with the NDT projects currently progressing or up for ballot are as follows: • Ballot: ISO/CD 16829 Non-destructive testing
— Automated ultrasonic testing — Selection and application of systems
• Ballot: ISO/CD 25108 Non-destructive testing
— NDT personnel training organizations
• Ballot: ISO/CD 11666 (Ed 3) Non-destructive testing
of welds — Ultrasonic testing — Acceptance levels
• Ballot: ISO/CD 17640 (Ed 5) Non-destructive testing
of welds — Ultrasonic testing — Techniques, testing levels, and assessment
• Ballot: ISO/CD 20601 (Ed 2) Non-destructive testing
• Ballot: ISO/CD 23279 (Ed 4) Non-destructive testing
of welds — Ultrasonic testing — Characterization of discontinuities in welds
MT007 Committee Members have also been invited to assist on the ISO/TC 44/SC5 Committee who are the lead representatives for testing and inspection of welds. We will be working closely with the Standards Australia Welding Committee which allows us to provide NDT expertise and knowledge to the Australian Welding and ISO Committee.
As we enter into the new Standards Australia systems and expert areas, it is believed this will allow the MT007 Committee to focus on up-and-coming Standards together with providing expertise to allied industries. Please contact me using the details below if you have any questions or require further information and I will reply at the first opportunity. Angelo Zaccari MT007 Standards Chairperson angelo.zaccari@outlook.com
of welds — Ultrasonic testing — Phased array technique for thin-walled steel components
Industrial Eye September/October 2026
11
AINDT NEWS
Condition Monitoring Training Centres Unlock the future of your career with top-tier condition monitoring training from trusted providers. These training centres have earned the endorsement of AINDT, aligning perfectly with the national syllabi approved by the AINDT Certification Board. This ensures that you receive the highest standard of education and training.
Wood – Asset Performance Optimisation A: Level 3, 171 Collins Street, Melbourne 3000 T: 08 6314 2000 or (08) 6314 2280 E: svt.bu.training@woodplc.com W: woodplc.com
To maximise your learning experience, AINDT recommends obtaining a copy of the training module—either directly from the training provider or by downloading it from the AINDT website. This will ensure you are well-prepared for your course.
Western Australia
For those seeking certification, it's crucial to successfully complete the specified training program and required training hours outlined in ISO18436. This is essential for achieving certification in your desired conditioning monitoring method, category, and industry sector. All examinations are conducted by the AINDT. For exam dates and further details, please contact AINDT via: federaloffice@aindt.com.au.
Elevate your skills and advance your career with the industry's best training and certification programs.
Victoria
Industrial Precision Instruments A: Unit 12, 634-644 Mitcham Road, Vermont 3133 T: 1300 781 701 E: training@ipi-inst.com.au W: ipi-inst.com.au IR Technology Australia A: 39-45 James Street, Lara 3212 T: 0418 569 698 E: erik.t@bigpond.com W: irta.com.au
University of Melbourne A: Parkville 3010 T: 03 9810 3348 E: claudine.evans@unimelb.edu.au W: unimelb.edu.au
12
ICM Training Solutions A: 45 Delawney Street, Balcatta 6021 T: 0419 993 233 E: rainingacademy@icmt.com.au W: icmt.com.au
SRG Training Academy A: 109 Bannister Road, Canning Vale 6155 T: 08 9232 0300 E: trainingacademy@srgglobal.com W: srgglobal.com
Wood – Asset Performance Optimisation A: Level 1, 240 St Georges Terrace, Perth 6000 T: (08) 6314 2000 or (08) 6314 2280 E: svt.bu.training@woodplc.com W: woodplc.com
Queensland
Advanced Infrared Resources Australia AIRA A: PO Box 372, Hervey Bay 4655 T: 0467 565 836 E: jeff@irtau.com.au W: irtau.com.au Machinery Diagnostics Institute A: 16 Wheeler Avenue, Gracemere 4702 T: 0499881 294 E: training@mcsturbo.com W: mdiaustralia.com SRG Training Academy A: 7 Brisbane Road, Riverview 4303 T: 07 3816 5500 E: training@mcsturbo.com W: mcsturbo.com
Wood – Asset Performance Optimisation A: Level 20, 127 Creek Street, Brisbane 4000 T: (08) 6314 2000 or (08) 6314 2280 E: svt.bu.training@woodplc.com W: woodplc.com
Industrial Eye September/October 2026
AINDT NEWS
Authorised Qualifying Bodies AQBs are authorised to offer AINDT-approved training and initial and recertification examinations in any Australian state, at any time throughout the year. The AINDT also conducts scheduled examination rounds twice yearly, with dates advertised in The Industrial Eye and the AINDT e-newsletter. While the AINDT strives to notify certificate holders of impending certification expirations, it remains the responsibility of the certificate holder to initiate the renewal and recertification process before their certification expires. Please note that late fees apply to overdue certification applications.
Victoria
ATTAR T: 03 9574 6144 E: training@attar.com.au W: attar.com.au
NDT methods, levels, and industry sectors offered: • Computed and Digital Radiography 2, 3
• Ultrasonic Testing 1,2,3 Welds, Casting, Wrought, • Aerospace, Thickness
• Radiographic Testing Level 1, Level 2 and 3 Welds
(ISO 9712) Full Matrix Capture Level 2 Welds (ISO 9712) • Magnetic Particle Testing 1,2,3 Multisector, Aerospace • Penetrant Testing 1,2,3 Multisector, Aerospace • Eddy Current Testing 2,3 Multisector, Aerospace • Magnetic Flux Leakage 2 • Tank Bottom Testing • Phased Array levels 2 and 3 Ultrasonics 2 Multisector • Visual/Optical Testing 2 Multisector • Time of Flight Diffraction (TOFD) levels 2 and 3 Welds • Heat Treatment • ISO 9712 UT Level 2 Corrosion/Erosion Detection and Mapping (CDM)
Western Australia
ATTAR T: 03 9574 6144 E: training@attar.com.au W: attar.com.au
NDT methods, levels, and industry sectors offered: • Computed and Digital Radiography 2, 3
• Ultrasonic Testing 1, 2,3 Welds, Casting, Wrought, • Aerospace, Thickness
• Radiographic Testing Level 1, Level 2 and 3 Welds
(ISO 9712) Full Matrix Capture Level 2 Welds (ISO 9712)
• Magnetic Particle Testing 1,2,3 Multisector, Aerospace • Penetrant Testing 1,2,3 Multisector, Aerospace
• Eddy Current Testing 2,3 Multisector, Aerospace • Magnetic Flux Leakage 2 • Tank Bottom Testing
• Phased Array 2, 3 Ultrasonics 2 Multisector • Visual/Optical Testing 2 Multisector
• Time of Flight Diffraction (TOFD) 2, 3 Welds • Heat Treatment
• ISO 9712 UT Level 2 Corrosion/Erosion Detection
and Mapping (CDM) NDT methods, levels, and industry sectors offered: • Ultrasonic Testing 1,2 Welds • Magnetic Particle Testing 1,2 Multisector • Penetrant Testing 1,2 Multisector • Phased Array Ultrasonic Testing 2 Multisector
Queensland
Protecs Global T: 07 3492 9213 E: hamed.madani@protecsglobal.com.au W: protecsglobal.com.au
NDT methods, levels, and industry sectors offered:
• Ultrasonic Testing 1 ( General Engineering) 2 Welds • Magnetic Particle Testing, 2 Multisector • Penetrant Testing, 2 Multisector
Industrial Eye September/October 2026
13
INDUSTRY NEWS
Thermography In Action The Importance of Infrared Inspections on Electrical Equipment
BY JEFF ERICHSEN, DIRECTOR/FOUNDER, IIAT CATEGORY 3 ADVANCED INFRARED RESOURCES TRAINED THERMOGRAPHER CATEGORY 2 AINDT CERTIFIED ELECTRICAL THERMOGRAPHER #5136
The importance of infrared inspections on electrical equipment is often downplayed and even often ignored until it is enforced by either a change in asset management strategy or by an insurer.
Fortunately due to the implementation of ISO 550001 and through the diligence of industry bodies such as the Australian Professional Thermography Association (AUSPTA) and the Australian Institute of Non-Destructive Testing (AINDT) many asset owners and insurers alike are now seeing the value of the implementation of regular infrared inspections.
Trained, Certified and Experienced
The difficulty is that the person who is often engaged by these organisations is not a trained, certified and experienced thermographer, but an maintenance technician who is provided with, or purchases a low end infrared imaging device that is not fit for purpose. Let’s unpack the three necessary parameters of a good thermographer: trained, certified and experienced. These three parameters are often unknown to the asset owner or insurer and are often used incorrectly.
Trained Thermographer
A trained thermographer is deemed as a person who has completed and passed, at a minimum, a Category 1 course that is written to the ISO standard 18436-7 and that course has been certified by a JAS-ANZ appointed third party body such as the AINDT. Passing this certified course, does not mean the thermographer is certified.
Certified Thermographer
A certified Category 1 thermographer according to ISO 18436-7 is one who has completed an approved Category 1 thermography course and passed the end of course exam, has passed another 3rd party exam, has completed a minimum of 12 months of practical thermography and has submitted 2 recent reports for review to the AINDT.
When all of these parameters are verified and accepted, then the thermographer is deemed as certified. This process is very similar for each category of 14
thermography, though the time in years is an additional 12 months for Category 2 and 2 more years for Category 3 (Minimum 16 hours Thermography-based CM per month).
Experienced Thermographer
Depending on the mentoring process, completing the minimum time periods does not always equal experience and the beginner thermographer should always ensure that they have a mentor to check their diagnosis, prognosis and recommendations on a regular basis as new types of faults are found. I can attest that Infrared Thermography is, as in any discipline, a life-time of learning. Industrial Eye September/October 2026
INDUSTRY NEWS
Camera Quality
Finally, as far as parameters go we should talk about camera quality.
It is generally accepted throughout industry that to provide the minimum geometric resolution and measurement capability for electrical inspections, the thermal imaging device should have a minimum detector array size of 320 x 240 pixels.
all product into the production plant and if this system were to fail, the complete operation of the production plant would halt, costing hundreds of thousands of dollars per hour. As shown in the digital image, no visible defects are evident on the load side of the contactor or the overload circuit.
These details are outlined in the AUSPTA electrical scope of work, which was developed by leading Australian industry thermographers. The full document can be found by following this link: www.auspta.asn.au/ resources/PublicDownloads/AUSPTA%20039.%20 Electrical%20Scope%20of%20Work%20V2.2%20 reviewed%2029-09-2023.pdf
It is also recommended that the device has manual focus and the ability to change lenses. These additional parameters ensure the electrical thermographer will have the capability to deliver clear images with accurate temperature calculations in most situations they find themselves in.
When a person is engaged who does not satisfy the parameters above or have the correct equipment, it can lead to this person not seeing low level faults and/or the misdiagnosis of faults at best, or at worst, a complete failure to identify a critical fault that will lead to a catastrophic failure if not attended to.
In my experience, the latter does not occur too often due to the nature of thermal imaging equipment which by function usually shows impending catastrophic failures as “glowing hot” in the colour pallet as bright orange, red or white (depending on the palette used) which intuitively informs even an inexperienced operator that something is wrong.
Load side of contactor red phase.
The challenge in this situation for the beginner thermographer is that as seen in Image 2 below, the thermographer is observing a bus bar connection to the contactor where the bus bar and the fastener are both low emissivity objects which means they are more reflective of thermal energy than they are emissive. This often means that if the thermographer is inexperienced and has their thermal imager set in auto mode (this is where the imager automatically sets its span to suit the environment it is viewing) then the anomaly may be normalised as per the image 2 below.
In this case study, we are going to discuss a fault that should be relatively easy for the novice Category 1 Certified thermographer to “find” but could easily be misdiagnosed as one of the electrical thermographers main challenges: Reflection.
Challenge
IIAT was requested to conduct Thermal Surveys on the electrical Distribution boards (DBs) and the motor control circuits (MCCs) at a client’s material production plant in central Queensland to decrease the risk of any unplanned breakdowns. Upon conducting the inspection, several thermal anomalies were identified, With the most severe anomalies evident on the red phase on the load side of the contactor and overload circuit on the plant feed conveyor shown in image 1 below. The plant feed conveyor system is the main conveyor that transports Industrial Eye September/October 2026
Fault in auto.
When the thermographer changes the camera settings to manual mode and sets the span correctly, he or she is able to now clearly define the problem as an internal connection issue within the contactor as the thermal gradient is observed as emitting more energy from 15
INDUSTRY NEWS
behind the plastic case of the breaker and conducting outward toward the connection as shown in image 3 below.
Load side of contactor red phase in manual mode.
An experienced thermographer also understands that as the plastic cover of the breaker is an insulator, then the problem inside the breaker is likely much worse due to the decrease in energy conducting through the case and along the bus bar. The next challenge for the thermographer is having the confidence (due to experience) in calling for a shutdown of a piece of equipment that they know, will cause hundreds of thousands of dollars in downtime to fix the fault immediately as the severity of this fault requires. When making this type of call, the thermographer often is subject to scrutiny and backlash from maintenance and production management which can be both confronting and daunting. In this case our field thermographer stood his ground and was adamant that the fault needed to be addressed immediately. The maintenance and production management reluctantly obliged and organised a direct replacement part so that the actual downtime which included shutdown, isolation, removal, fitment of the new part, re-energisation and re-starting was minimal.
The contactor was immediately disassembled on request of the thermographer and the digital images below clearly show that there was damage and oxidisation of the internal connections of the breaker which would have eventually have led to a catastrophic failure. After being in service for more than an hour, the component was re-imaged to ensure the fault had been rectified. This is of course another step in worlds best practice that many clients often wish to skip, however our business always lobbies for the completion of this step to ensure rectification has occurred. Fortunately, some insurance companies are now advocating for this final step to be completed on all
16
faults flagged for repair in a thermography report as they believe it dramatically reduces their insurance risk.
Conclusion
This case study is one of many instances where our business has identified and assisted in addressing critical faults that would have led to catastrophic failures. Infrared inspections of electrical systems are the cheapest and most effective insurance for most production related businesses. .
Industrial Eye September/October 2026
RENEW YOUR MEMBERSHIP RENEW FOR REWARDS: STAY A STEP AHEAD WITH 2026-2027 AINDT MEMBERSHIP Whether you're looking to enhance your knowledge, expand your network, or influence industry standards, AINDT is your gateway to success. Connect with top professionals and thought leaders in an environment that celebrates innovation and progress. Just some of the member benefits are outlined below.
AINDT MEMBERSHIPS ARE DUE BY 30 JUNE
Regular editions of the AINDT Journal (6 per year) Substantial discounts on certification fees and expenses Access to our online portal and resources Eligibility for exam and industry service awards A host of networking opportunities, including branch events, workshops, seminars, and our conference Exclusive Corporate Member benefits like free and discounted advertising rates, and technical advice
RENEW NOW >>>
aindt.com.au
AINDT NEWS
Queensland Branch Update Queensland AGMs
The Queensland Branch recently hosted its 2026 Annual General Meeting in both Brisbane and Gladstone. It was a fantastic evening, made possible through the generous support and sponsorship of Evident and, of course, the great company of everyone who attended. Special thanks to Sean Fogerty for his excellent presentation and very articulate speech, as well as for doing the honours in presenting Evident’s lucky door prize.
Thank you to Evident and to everyone who travelled and participated in both Brisbane and Gladstone. Your continued involvement and support of the AINDT community is sincerely appreciated.
AINDT Exam Awards
We would also like to recognise Smartchem for their ongoing support of the AINDT exam awards. Congratulations to Warrick Pozzan and Ryan Imrock on your well-deserved achievements. Unfortunately, Ryan was unable to attend on the night, so his award will be making its way to him by mail.
Upcoming Events
Looking ahead, the team is working towards delivering three technical events and at least one social event before the end of the year. Details are still being finalised, so keep an eye on LinkedIn for upcoming announcements. Personally, I would also like to acknowledge the dedication and commitment of our Council members, both past and present, and warmly welcome our new members.
To all our financial members, thank you for your ongoing support. I encourage you to take full advantage of everything AINDT has to offer over the coming year. If you haven’t yet renewed your membership, there’s still time!
Here’s to another productive and enjoyable year for the AINDT Queensland Branch. Steve Kennedy President, AINDT Queensland Branch
18
Industrial Eye September/October 2026
AINDT NEWS
South Australia Branch Update The South Australia Branch held its Annual General Meeting in mid-September at Laneway Social, with members coming together for an evening of reflection, recognition and renewal. Branch Vice-President John Greig opened the night by thanking our generous sponsors: Platinum sponsors ASC, Red Earth, E 33 Pty Ltd and Evident Australia, and Silver sponsor Bureau Veritas. Their support made the evening possible, and each Platinum sponsor also contributed a door prize. The President's report looked back on a busy year. Branch Council met throughout the year, and the Branch hosted a booth at the SA Job Fair at Wayville Showgrounds in May, with thanks to the members who volunteered their time. NDE Solutions hosted a Volio drone tech night in November, and the Branch has begun early talks with TAFE SA on a Certificate IV pathway.
Members also heard an update from Federal Council, covering the national budget, progress on the rail testing scheme, the constitution review, and new colour vision test requirements to align with the updated ISO 9712. Membership benefits were also discussed, including portal updates, and faster certification services.
A highlight of the night was celebrating South Australia’s 2025 award success, with Dennis Gare recognised with the LMATS Radiographic Award for the best overall result in the AINDT Level 2 Radiography examination. The meeting closed with the election of the 2026-2027 Branch Council. Andrew Morris steps into the role of President, with John Greig as Vice-President, Matt Hobbs as Treasurer, Nick Hart as Secretary, and Pawel Banda as Federal Member. Tyson Jenke, who stepped down as President, continues as Past President. The Branch thanks Tyson for his leadership, along with all outgoing and continuing council members for their service.
Thank you to everyone who attended and helped make it such an enjoyable night. We look forward to seeing you at our upcoming events.
Industrial Eye September/October 2026
19
AINDT NEWS
Victoria and Tasmania Branch Update Celebrating a Year of Technical Development and Member Engagement BY MIRO KATOUZI, PRESIDENT – AINDT VICTORIAN/TASMANIAN BRANCH
The 2026 AGM brought members and industry colleagues together in Docklands to recognise technical achievement, reflect on the 2025–2026 year and continue building a practical, connected NDT community across Victoria and Tasmania. The AINDT Victoria and Tasmania Branch brought members and industry colleagues together for its 2026 Annual General Meeting on Friday 21 August at Urban Alley Brewery in Docklands. The evening combined the formal AGM with dinner, awards, discussion and networking, providing an opportunity to recognise individual achievement while reflecting on another active year for the Branch. The program was deliberately structured to allow plenty of time for members to socialise and engage with fellow professionals before and after the formal AGM proceedings.
AINDT Victoria and Tasmania Branch councillors at the 2026 AGM.
LMATS, the Gold Sponsor of the evening, supported the event and also generously supplied a number of door prizes, including a drone. The Branch sincerely thanks LMATS for its contribution and ongoing support of the local NDT community.
Recognising Technical Achievement
A highlight of the evening was the presentation and recognition of the Victorian and Tasmanian recipients of the 2025 AINDT examination awards. Curtis Thorburn achieved outstanding results across three Level 2 examinations: the SmartChem Award for the highest percentage pass mark in General Penetrant Theory, the Chemetall Penetrant Award for the highest mark in the Level 2 Penetrant Practical Examination, and the Chemetall Magnetic Particle Award for the highest mark in the Level 2 Magnetic Particle Practical Examination.
William Spicer received the Endetek Eddy Current Academic Excellence Award for the highest overall result across the General, Specific and Practical components of the AINDT Level 2 Eddy Current examination. Michaela Neville was recognised for the highest result in the Level 2 phased array ultrasonic Specific and Practical examination. Jacob Burton received the Duerr NDT/EN DE TEK RT CR/ DR Award for achieving the highest overall percentage pass mark in the AINDT Level 2 examination for 2025. The Branch congratulates all of the award recipients on their achievement and the high level of technical capability represented by these results.
AINDT Victoria and Tasmania Branch councillors at the 2026 AGM.
Winner of one of the door prizes supplied by AGM Gold Sponsor LMATS, with her new drone. 20
Jacob Burton receiving his 2025 Duerr NDT/EN DE TEK RT CR/DR Award from Stuart Norman. Industrial Eye September/October 2026
AINDT NEWS
At Federal Council level, the Branch was represented by Paul Trigg, Pranay Wadyalkar and Miro Katouzi. Issues discussed during the year included certification and recertification, practical examination matters, career pathways, member engagement and wellbeing, communication between the Board and Branches, and better coordination between state Branches.
The AGM also provided members with an opportunity to raise questions and exchange views directly with Branch councillors, continuing the open discussion and member engagement that the Branch aims to encourage.
William Spicer receiving the 2025 Endetek Eddy Current Academic Excellence Award from Victorian/Tasmanian Branch President Miro Katouzi.
A Year Focused on Practical Member Value
Throughout 2025–2026, the Branch continued to place emphasis on activities that provide direct professional and technical value to members.
One of the more distinctive initiatives was the online “Mental Health in the NDT Workplace” session, presented by Matt Glover and Cam Semmens. The session addressed issues including stress, burnout, shift work, isolation and psychological safety – challenges that can be particularly relevant to people working in inspection and field-based environments. Technical development remained central to the Branch program. On 26 May 2026, the Branch worked with Evident to deliver a practical technical night featuring the OMNISCAN X4 128, including live demonstrations, practical examination preparation, customised overlays, matrix probes and approaches to data management. The program also included an event with Wabtec Inspection Technologies Australia covering the NORTEC 700 Eddy Current Flaw Detector and Eddy Current Array fundamentals, applications and live demonstrations.
Another important member initiative was the introduction of certificates of attendance for eligible technical nights. These certificates provide evidence that members can use when claiming applicable professional-development credits under AINDT’s Structured Credit System for renewal and recertification, strengthening the link between Branch participation and continuing professional development.
Engagement beyond the Branch
Several Branch councillors and members attended the AINDT Summit 2026 in Newcastle from 20–22 April under the theme “The Power of Inspection”. Their participation strengthened connections with technical developments and the broader NDT, condition monitoring and inspection community.
Industrial Eye September/October 2026
Members and Branch councillors during the question-and-answer and discussion session at the 2026 AGM.
Membership and Social Connection
Total Branch membership grew by approximately seven per cent during the year, from 214 members in June 2025 to approximately 230 members in June 2026. Social activities continued alongside the technical program. The annual Family Christmas BBQ, held at Chesterfield Farm in Scoresby in December 2025, brought members, partners and children together in a more relaxed setting and provided an opportunity for families to connect outside the normal work environment. Looking Ahead
The Branch’s priorities for the coming year remain focused on maintaining a consistent practical technical program, supporting certification and professional development, strengthening career pathways, increasing engagement with employers and educational institutions, improving member communication and visibility, and extending access to activities across both Victoria and Tasmania. The progress achieved during 2025–2026 would not have been possible without the time and contribution of Branch councillors, volunteers, presenters, sponsors and members. The Victoria and Tasmania Branch looks forward to continuing that momentum and creating further opportunities for technical learning, professional development and connection across the NDT community.
21
AINDT NEWS
Western Australia Branch Update The AINDT Western Australia Annual General Meeting (AGM) was held in late July at the impressive rooftop bar at Reveley on the Elizabeth Quay Waterfront. There was a really great buzz around the event with over 100 attendees consisting of a mix of members, nonmembers, member companies and industry experts who all mingled, networked and enjoyed the fantastic food and drinks on offer throughout the evening. As part of the formalities of the evening, Branch President Josh Wilkinson conducted a review of the Branch activities over the year and provided a Membership Report. Plus, Mike Needham provided his usual succinct Treasurers Report.
As always, these events wouldn’t happen without our generous sponsors, so a huge thank you to Applus, LMATS and Waygate Technologies. All sponsors provided fantastic door prizes that were very well received by the winners.
22
Industrial Eye September/October 2026
AINDT NEWS
Thank you to all the attendees who made it a very enjoyable evening and we look forward to seeing you all next year. The event closed out a very positive year for the Western Australia Branch of AINDT, while also looking ahead to a positive year of engagement with our members.
Industrial Eye September/October 2026
23
INDUSTRY NEWS
Northrop Grumman: Keeping RAAF Aircraft Airborne. And a Great Career Choice. Northrop Grumman Australia has been a growing part of Australia’s Defence community for over twenty years
The 800 strong team partners with the ADF to deliver innovative yet pragmatic solutions across all areas of Defence including Aeronautics, Mission Critical Systems, Space and Guided Weapons. As part of the global Northrop Grumman organisation which numbers over 100,000 employees across four continents, the team is able to draw on world-class capabilities whilst enjoying a reputation for local expertise and understanding. One of the top three aviation sustainment businesses in Australia, Northrop Grumman teams provide longterm maintenance support to key RAAF aircraft fleets based predominately across South East Queensland, Canberra, Katherine and Adelaide; each fleet playing a vital role for the RAAF. The KC-30A Multi-Role Tanker Transport, for example, performs airborne refuelling of a range of allied partner aircraft. It also provides longhaul transportation of ADF personnel and has up to 34 tonnes of underfloor cargo capacity.
The C-27J Spartan Light Tactical Fixed Wing aircraft, designed to operate from unsurfaced airstrips, forms a critical airlift capability for RAAF and aid to humanitarian 24
Industrial Eye September/October 2026
INDUSTRY NEWS
missions in remote locations. Five Special Purpose Aircraft are configured to enable Government and VIPs to continue business while travelling to attend international forums and conduct state visits often at short notice. And the new MQ-4C Triton uncrewed Intelligence, Surveillance & Reconnaissance aircraft, able to fly more than 24 hours at a time, above 50,000 feet in altitude and with an operational range of 8,200 nautical miles provides real-time ISR over vast ocean and coastal regions.
Non-Destructive Testing Technician What’s Your Possible? RAAF Base Amberley As part of one of the world’s largest defence companies, and a leading provider of aviation sustainment services in Australia, our Sustainment and Modernisation teams provide Through Life Support for the RAAF’s Fixed Wing aircrafts ensuring they are safe and mission ready. We’re looking for an aviation professional with strong NDT experience and a commitment to quality and safety. Fixed-wing experience is highly regarded, along with exposure to multiple NDT methods and certifications. The profession is rapidly evolving. Digital inspection technologies, advanced imaging systems and increasingly sophisticated maintenance programs are creating opportunities for technicians to expand their technical capability. This role offers you that opportunity, including progression towards Level 3 NDT qualifications. In return, we offer a range of industry-leading benefits, professional development and the chance to progress as we grow our business in Australia. Find out more here.
Industrial Eye September/October 2026
Whilst each of these platforms are maintained by dedicated on-site teams, subject matter experts also work across all parts of Northrop Grumman’s maintenance function to ensure quality, knowledge, compliance and, above all, safe practices are embedded. That’s where the organisation’s growing Non-Destructive expertise comes in. The company is committed to developing its NDT team and is currently looking for an NDT Technician to potentially work across its portfolio investigating real aircraft defects, each bringing different challenges, whilst also supporting others on their NDT journey. So strong aviation experience, ideally within Defence and utilising multiple inspection methods will be important. And, as the work involves close collaboration with Civil Aviation Safety Authority/Defence Aviation Safety Authority Licensed Aircraft Maintenance Engineers and engineering teams, an engaging approach as a natural communicator and a commitment to clear processes will be vital. Safe and serviceable aircraft outcomes are after all critical. Every inspection underpins mission success and safety. Northrop Grumman is worldleading, innovative and highly established. However, the company is also well respected for its ethical approach. Doing the Right Thing is a company value, and Everyone Matters a cornerstone of its employment proposition in Australia. Check out ngc.com/ Australia or see the NDT Technician advertisement in this issue.
25
TECHNICAL ARTICLE
Reflections on NDT Personnel Certification in Australia When I became NATA’s NDT Field Manager in 2000, I did not realise that I would have a front row seat in watching a significant industry transformation unfold. BY BRETT HYLAND, STAKEHOLDER ENGAGEMENT MANAGER, NATA
This is a much-abridged version of a talk given by the author at the AINDT Summit held in Newcastle in 2026.
My earliest engagements with managers of NDT facilities forcefully impressed upon me that the NDT industry was not in a happy place at that time, with competition driving down quoted rates to the point where it had become extremely difficult to retain skilled personnel or to invest in the training of new personnel. By way of background, for those not old enough to recall, AINDT had offered Technician and Technologist qualifications for decades prior, with moderate levels of adoption by industry. However, in 1997, AINDT introduced a new certification program based on AS 3998 (itself based on an as-yet-unpublished version of ISO 9712). This represented a major change since, unlike the earlier qualifications that were effectively held for life, the new certification required periodic renewal and re-examination. From the perspective of many practitioners, there was little incentive to move from a lifelong qualification to a certificate that required continuing effort and expense, particularly when qualifications were not usually demanded by clients in any case. Adoption of the new standard was therefore muted, to say the least.
This stalemate might have continued, except that the Australian standards for magnetic particle and penetrant testing were being revised during the late 1990s to require method-specific operator qualifications. Existing Technician and Technologist qualifications were explicitly permitted, but new entrants to the industry would henceforth need formal certification to test to these method standards, since the lifelong qualifications were no longer being offered by AINDT. My predecessor at NATA, Jan Chamberlain, had notified the NDT industry of a grace period for phase-in of the new rules, but most companies had not acted by the time the cut-off approached. The unenviable task of advising accredited NDT laboratories that NATA would henceforth raise nonconformances where personnel did not meet the qualification requirements contained in the relevant testing standards now fell to me. The response was 26
immediate and in December 2000 I found myself facing a rather agitated audience alongside AINDT Certification Board Chairman David Barnett and Standards Australia MT007 committee chair Charles Pope. There was not a lot of joy for the audience that evening.
I made clear that NATA had an obligation to assess laboratories against standards, exactly as they are written, if these are included within the accredited scope. Charles Pope for his part contended that Standards are developed through industry participation leading to consensus outcomes so, if audience members wanted different outcomes, they would need to participate actively to drive the standards-development process in different directions.
Ultimately, the enforcement of the surface-method qualification requirements would proceed and, unsurprisingly, it produced an unprecedented increase in demand for penetrant and magnetic particle certification. This placed considerable pressure on AINDT, which at that time operated with very limited paid resources and depended heavily on volunteers to administer certification, examinations and technical records.
The workload was substantial, and there were genuine concerns as to how long the organisation could continue to depend upon the self-sacrifice of a relatively small number of office-holders and other volunteers. Yet, it was the extraordinary growth in certification activity that would eventually generate the stable revenue base that would allow AINDT to develop into the financially sustainable and professionally-run organisation that we know today. A parallel development concerned technical control within accredited NDT laboratories. ISO/IEC 17025 required laboratories to maintain effective technical control, but applying this concept to historical NDT laboratories was not straightforward. On my early assessments, technical control appeared dispersed among branch managers, operations supervisors, technicians in the field and the personnel who had originally written the test procedures.
Industrial Eye September/October 2026
TECHNICAL ARTICLE
It was genuinely difficult to identify the person who could be regarded as holding technical authority for a method. What had been lacking was a formal responsibility description for NDT Level 3 practitioners, such as that provided within the new AS 3998 standard. NATA’s interpretive requirements would eventually be revised to make clear that the person exercising technical control over an NDT method was expected to hold appropriate qualifications, such as Level 3 certification. Over time, a clearer understanding emerged of the complementary relationship between AS3998 (later ISO 9712) personnel certification and ISO/IEC 17025 laboratory accreditation. Certification provided confidence in the technical skill of individuals, while accreditation considered how these skills are harnessed within laboratory systems and technical processes to deliver competent testing outcomes AINDT and NATA each recognised the value of the other’s role without attempting to take over the other’s processes. There were a few other developments I can recall from that time that also had relevance to the development of the Institute. Huge oil and gas infrastructure projects throughout the noughties greatly increased demand for certified NDT personnel, further helping to expand and stabilise the AINDT’s revenue base. At the same time, the AINDT successfully pursued JAS-ANZ accreditation for its personnel certification program, strengthening confidence in its certification processes while opening a pathway for international recognition of operators certified by AINDT. During my time, the Certification Board itself was also split into separate Boards for Condition Monitoring and NDT. All up, I served on the Certification Board for 21 years. Looking back, what stood out most clearly was the Industrial Eye September/October 2026
shared commitment to providing Australian technicians with credible, high-quality qualifications. There were many internal disagreements about approach and implementation, but the shared higher objective usually allowed a sound outcome to prevail. In my view, today’s professional Institute and mature certification system were built upon the technical knowledge, persistence and generosity of many past office-holders, most of whom were volunteers. Their contribution should remain part of the industry’s collective memory.
About the Author: Brett Hyland
Brett Hyland is NATA’s Stakeholder Engagement Manager and a recognised expert in product and asset compliance.
He has spent decades working with industry and government stakeholders on policies relating to testing of products and assets.
Over his career, Brett has been a prominent contributor to standards development within Australia, including the MT 007 Committee on Non-Destructive Testing of Metals and Materials and he is a recipient of the Australian Institute for Non-destructive Testing JH Cole Award for his significant contributions to the NDT industry.
27
TECHNICAL ARTICLE
Is it Time to Include Human Factors Education for NDT Technicians? Knowledge of Human Factors (HF) largely falls outside traditional NDT technical training. The scientific physical principles which underpin NDT qualification and certification in all methods gives the technician an understanding of how and why a particular NDT method works, or doesn’t work, as intended. BY COLIN HOCKINGS
The nearest the NDT certification standards come to Human Factors is requiring vision testing which enters the area of the technician’s physical condition and this is certainly part of Human Factors considerations (1). Papers and presentations of Human Factors specifically applicable to NDT go back at least to the 1980s. This article will not go into the origins of the study of Human Factors. The reader can source many reports on the subject. However, to provide some context, the first formal collaborative research groups were the Ergonomics Research Society in the UK in 1950 which is now the Chartered Institute of Ergonomics and Human Factors, followed by the Human Factors Society of America formed in 1957. (2)
Some Background
The safety significance of NDT is self-evident by the industry and regulatory standards which mandate and govern inspections. And the object of any HF education in NDT would be to improve reliability of those inspections, i.e. less errors.
There has certainly been an up-tick in academic investigations into Human Factors and Error Management in NDT, with some “trigger” events along the way which have stimulated this research (3). Human Factors is of genuine interest to power generation, road and rail transport, public health, aerospace, oil and gas and other sectors to analyse and improve personal performance in a wide variety of working environments. NDT service companies intersect with most of these sectors and should not exclude themselves from an understanding and application of Human Factors in their work.
Arguably, the first substantial attempt to assess realworld reliability of NDT inspections is the 1978 USAF sponsored study (4) where nearly 300 technicians across 21 different sites inspected large structural samples containing fatigue damage using various NDT methods. Aside from fluorescent penetrant, the methods used in the program demonstrated significant difficulty achieving a 50% probability of detection for a 1/2inch (13mm) crack size with a 95% confidence level. The reliability of NDT inspections remains a focus in 28
industries where the criticality of plant and equipment is fundamental to safe and profitable operation.
A Definition
Before going further it will be helpful to settle on a definition of Human Factors education for the reduction of errors. Of the many definitions offered, I prefer the simple one proposed by John Wilson (5). “Understanding the interactions between people and all other elements within a system, and design in light of this understanding.” The inclusion of “all other elements” goes beyond the ergonomic man-machine interface to encompass the full complexities of the working environment. This wider view will take HF into the organisational level, meaning that HF education of the NDT technician alone is unproductive unless the employer and maybe even the client also have an understanding of the reasons for applying HF considerations to NDT inspections. Human factors could be considered as the interaction between: • People and Machines • People and People
• People and Procedures
• People and the Environment
Automation and Artificial Intelligence would appear to be the answer to all these problems. The removal of “People”. But this is not always possible or preferrable. Some would argue that the higher the degree of automation the greater the benefit when it works, but the greater the cost should it fail. (6)
Whilst automation and the capability of NDT equipment and processes have achieved significant advances in recent times, and should continue to do so, dispatching NDT technicians to the client’s site with portable test equipment will be a feature of the industry for some time to come. This makes for an opportunity to improve inspection reliability through Human Factors education. So what tasks remain with people? • Use, operation
• Design and development of new technologies
• Monitoring automated systems and processes
Industrial Eye September/October 2026
TECHNICAL ARTICLE
• Automation gaps (e.g. complex decision-making)
And what tasks are transferable to automation or AI? • Complex computational tasks
• Routine, monotonous and repetitive tasks • Time-consuming tasks
• Physical or dangerous tasks
Practicalities
NDT work is often characterised by high workload in limited timeframes which challenge the technicians and those who plan the work. A technician who is HF aware is more likely to recognise and appreciate the significance of foreseen and unforeseen changes to their work environment.
As an example, the pressure to extend the daily work time on site is common and often justified. An organisation which applies HF considerations to its workforce planning will have employees with the skills to identify and assess the potential risks to the inspection tasks caused by extending the shift. They could then apply strategies to mitigate the adverse effect of such things as an increase in technician fatigue or changing environmental effects of variable ambient temperatures and lighting.
Human Factors Models
Like most safety regulators, the Federal Aviation Administration in the United States (FAA) has produced a range of guidance material to assist the industry to understand and apply Human Factors in commercial and private aviation (7). Its model of HF includes; cognitive science, safety engineering, anthropometry, experimental psychology, clinical psychology, industrial engineering, educational psychology, organisational psychology, medical science and computer science. This is quite a list and while an in-depth knowledge of each is not a sensible objective of HF education, an appreciation that there are a multitude of variables which can degrade inspection reliability is desirable and more importantly an ability to recognise when any of these are influencing technician performance. The figure below shows the potential connections to be managed.
Group Characteristics: social influence, teamwork, human redundancy
Technology: equipment, design. human-machine interaction, human-automation interaction, usability
Task Characteristics: preparation, inspection procedure/ instructions, decision aids
Accidents Errors and Education
In my view, training is skilling a person to perform a task correctly. Education is more, it is skilling a person to also think critically. Knowledge of Human Factors has the potential to make a more capable and reliable NDT technician and therefore a more capable and reliable NDT organisation. The “Swiss Cheese” accident model by James Reason (9) is routinely embedded in Human Factors education along with other models of relationships between influencing variables (10). The Swiss Cheese model depicts slices of cheese representing barriers to errors which could be such things as inspector training, work procedures, off-site support, equipment control, task preparation and the like. Only when all the defences fail do the holes in the cheese align and an error can occur.
More specifically for NDT, a simplified version as suggested by D’Agistino (8) is;
Individual Differences: personality, abilities, decisionmaking strategies, motivation, memory, perception, attention, stress, workload, experience, gender, age
Organisational Factors: culture, safety culture, pressure, supervision, pre-and post-job briefing, work planning and coordination, communication, work hours, feedback, training Physical Environment: temperature, noise, time pressure, lighting, restricted workspace, body posture, distractions
Industrial Eye September/October 2026
29
TECHNICAL ARTICLE
In the early 1990s Gordon Dupont of Transport Canada developed a list of twelve Human Factors which could degrade personal work performance leading to errors (11). They are: Lack of Communication, Lack of Teamwork, Lack of Assertiveness, Complacency, Fatigue, Stress, Lack of Knowledge, Lack of Resources, Lack of Awareness, Distraction, Pressure and Norms. Some are self-explanatory while others may need fleshing out a little more. In situations where an error has occurred it is often the case that more than one of these factors were present.
For the NDT organisation which applies HF considerations to its operation it will be found to have policies and procedures for things like; managing fatigue, reviewing and simplifying inspection instructions, open communications and feed-back, ongoing education and employee engagement. What Next
Gordon Dupont’s list could be a workable starting point for a HF program suitable for the NDT industry. Identifiable traits and characteristics of each human factor can be developed and applied to realistic working environments. The objective for students is that they can recognise each and apply planned and improvised strategies to mitigate the risks to inspection reliability that they may pose. Human Factors education is not idealistic. It is quite achievable and can have good outcomes for individuals and organisations. Just like the positive changes in contemporary attitudes to workplace health and safety which have now become a routine part of the preparation and performance of NDT tasks. HF education enhances what could be described as “soft” skills and will promote improved situational awareness by employees making them even more effective in their assigned role.
References
1. Bertovic (2016). Human Factors in Non-Destructive Testing (NDT): Risks and Challenges of Mechanised NDT. BAM Berlin, ISSN 1613-4249
2. humanisticsystems.com/2018/02/25/humanfactors-and-ergonomics-looking-back-to-lookforward/ 3. Three Mile Island nuclear accident (1979) www.nrc.gov/docs/ML0402/ ML040280573.pdf Aloha Airlines incident report (1988) www.ntsb.gov/ investigations/AccidentReports/Reports/AAR8903. pdf
30
Piper Alpha offshore oil rig explosion (1990) UK HSE Report www.hse.gov.uk/offshore/piper-alphadisaster-public-inquiry.htm. 4. Lewis W.H. et al (Lockheed Georgia) USAF Technical Report; “Reliability of Non-Destructive Inspections”, SA-ALC/MME 76-6-38-1 5. Wilson, J (2014). Fundamentals of systems ergonomics/human factors. Applied Ergonomics, 45(1), 5-13.
6. Onnasch L, Wickens CD, Li H, Manzey D. Human performance consequences of stages and levels of automation: an integrated meta-analysis. Hum Factors. 2014 May;56(3):476-88.
7. FAA Advisory Circular 120-72A - Maintenance Human Factors Training. www.faa.gov/documentLibrary/ media/Advisory_Circular/AC_120-72A.pdf 8. D’Agostino, et al (2017). Review of Human Factors Research in Non-destructive Examination.
9. Reason, J. (1997), Managing the Risks of Organisational Accidents, Farnham, Surrey: Ashgate 10. Shell Model after Hawkins, F.H.: Human Factors in Flight, 2nd edn. Ashgate, Aldershot (1987), Pear Model after Johnson (FAA) and Maddox (Humancentric Technologies Inc. (2007)
11. Gordon Dupont (Transport Canada) Dirty Dozen” (1993)
About the Author: Colin Hockings Brett Hyland is NATA’s Colin Hockings is an AINDT Honorary member and has had a lengthy career in aviation maintenance including NDT, Safety and Regulatory Compliance, holding qualifications in each of these areas including a Masters of Safety Science (UNSW). He has held various safety and quality roles in large and small organisations where Human Factors were a part of the compliance framework.
He founded Aero Compliance Consulting in 2013 and continues to be involved in aviation and other industries.
Industrial Eye September/October 2026
TECHNICAL ARTICLE
Power of Process Control in Software Driven NDT Procedures The industry has long relied on traditional multi-page documents for NDT procedures. However, their length and text density frequently lead technicians to miss key process parameters and especially after revisions, resulting in non-conformities. Since 2010, the author has developed software-driven procedures to offer active process-control management of NDT operations. BY PRANAY WADYALKAR, MANAGING DIRECTOR, OMS SOFTWARE
Industry Benefits
What is a Procedure?
• Easier for testers for following the set procedure
A procedure is a specific series of actions or steps taken in a set order to achieve the desired objective consistently and correctly.
ISO 9712 Clause 3.27 defines a procedure as a description of all essential parameters and precautions to be applied when testing in accordance with standards, codes, or specifications. Both definitions highlight ‘consistently’, ‘correctly’ and ‘precautions’ as the key essentials required to achieve true process control.
Problem Statement
Most testing facilities continue to use traditional, multi-page lengthy procedures containing excessive text, which are often skipped, skimmed, or forgotten when prone to complacency. Revised procedures are occasionally communicated poorly, causing nonconformities (NCRs). Furthermore, traditional paper test record forms or basic Android input-output forms as part of the procedure fails to control processes, or prompting technicians adequately, or standardise data collection.
There are several examples of lengthy procedures including my own from some 15 years ago when I was writing lengthy document after learning from others. But I was wrong. My experience managing more than 300+ technicians indicate that detailed comprehensive procedures alone cannot prevent testing errors without active workflow enforcement.
Solution
Implement process control via software-driven procedures by digitalising the entire company workflow, not just the test procedure. Pre-configure and standardise data input while actively prompting essential parameters to NDT personnel.
Industrial Eye September/October 2026
Some of the benefits are:
protocols in the form of software UI (User Interface).
• Process control to eliminate errors, NCRs and rework,
thus increase quality and efficiency.
• Communicate digitally for revised procedures and
essential parameters via UI.
• Detailed report to the end client for reproducibility,
containing Standard's terminologies for all parameters in the form of UID (Unique Identification of parameter name).
• Digital data transmission to the end client for future
reference or repeating the test when any acceptable or undetected discontinuities grow.
• Remote analysis of test data (PAUT, TOFD, DR, ECA
files) by a L3 or other competent people from anywhere in the world.
Guide to Implement Effectively
• Implement process control as per your procedure and
the test record form in the UI.
• Prompt all essential parameters to NDT personnel. • Standardise data type for each parameter by
connecting reference libraries.
• Transmit data electronically via JSON or other
acceptable file formats (such as DICONDE or HDF)
The following guideline can be used to implement software-driven process control before, during, and after testing. 1. Essential JSA (Job Safety Analysis)
Personnel safety takes precedence. Digital systems must feature interactive, conditional JSA logic. For example, if a tester answers "No" for not knowing an emergency escape route, the workflow should halt, forcing them to conduct safe work method, record risks, hazards and control measures before further work. 31
TECHNICAL ARTICLE
2. Job Details To comply with ISO 17025, the UI must track active working dates. The test date is not just the date when the testing was conducted but the entire process from job start to end. Hence, the UI must include adequate process control to prompt whenever anybody attempts to change dates outside the activity date range.
Before the tester commences work, the UI must prompt personnel to discuss with work scope with the client and record any variations or any conflict of interest within the UI to comply with accreditation requirements. Frequently, clients provide special instructions for a job. Such special instructions shall be delivered to the tester via the UI so that testers the software can prompt personnel to read on their smart phone or tablets without a need to check their emails or accessing a server or going to their car to search the printed copy. This real time access for the testers will eliminate some of the common issues. 3. Job Technical Details
Technical details include test specification, test standard and related procedures which are essential for testers. Instead of relying on printed folders left in vehicles (which are frequently superseded), the UI must provide instant, one-click access to the latest test specifications, method standards, and acceptance criteria.
32
The UI shall display only approved testers, automatically flagging their expired vision assessments or five-year practical examinations or certifications. Many standards specify to include tester’s qualifications on test records and reports. Hence, instead of the typing some inconsistent text, the UI should automatically retrieve their standardised qualification certification text string from the database. This process control will ensure consistency across all reports. The UI shall have input boxes for selecting trainees working under the lead tester so that the database can generate a logbook to demonstrate experience for their AINDT certification. 4. Test Equipment
The UI must display input boxes for recording detailed instruments data as per the requirements of the test method standard and your procedures, for the purposes of test repeatability and reproducibility. Moreover, it must prompt the tester for essential parameters when missed. Safety comes first! Hence, the UI must prompt the user for checking electrical testing tag for their portable electrical equipment. Without checking this item, the UI shall not permit them to proceed to the next stage.
The UI must not display any A/N (Asset Number) if the test equipment is not calibrated or verified for the suitability for test. The procedure software must be intelligent to automatically retrieve all essential details for the equipment used. For example, in UT, the UI should retrieve calibration block type and its verification Industrial Eye September/October 2026
TECHNICAL ARTICLE
expiry date after the tester selects the unique A/N. Similar protocol shall be for reference or simulation blocks in PAUT, TOFD or CR-DDA.
Similarly, after the tester selects A/N for transducers, the UI shall auto-retrieve all details such as its crystal type, dimensions, frequency, angle and the corresponding calibration expiry date. For PAUT, it shall include elements and wedges details as well to comply with standards. Essentially, the process control implemented in the software driven procedure UI should assist testers to save their time and to capture consistent data for every test instrument and equipment used for testing. 5. Test Conditions and Settings
All standards specify to record several test technique related parameters and test conditions. Hence, the UI shall prompt testers to capture surface condition, preparation, scan plan compensation gain, transfer correction, gain, damping, scanning sensitivity, etc. For PAUT, it shall prompt to upload files for focal laws and calibration data for velocity, wedge delay and TCG. Instead of the tester writing some non-standard terminologies for surface condition, the UI should display images of weld surface condition (as per AS 2207 SP1 to SP4.) The UI should also display various scanning methods as per your procedure for various Industrial Eye September/October 2026
standards. For example, scan plans illustrating probe positions as per AS 2207 can be displayed on the UI. It can also include a table for all essential test parameters such type of transducer types, probe positions, scanning sensitivities and evaluation criteria as per your procedure.
When clients require testing across different standards (such as AS 2207 and ISO 17640), the UI shall simultaneously display specific scan plans and sensitivity requirements to ensure testing is conducted as per the requirements of each standard. Considering varying designations for probe positions, the UI shall display the standardised terminologies for selecting probe positions so that the test can be replicated in the future if an acceptable discontinuity or missed discontinuity grow in service. 6. Test Items Identification
Most standards do not specify to include client specific part details such as Weld type, process, position, welder name, spool number, drawing or WPS number. Hence, the procedure UI shall be pre-configured to accommodate each client’s requirement separately so that the UI can prompt testers as part of the process control to include all specified details as per the client specific procedure. 33
TECHNICAL ARTICLE
7. Test Items Photos and Documentation Geometry constraints (such as tee-junctions or confined corner welds) often restrict 100% test coverage. Hence, the UI should prompt testers to record restrictions and capture photographs of test areas to prove what was tested for the unforeseen circumstances. The UI shall facilitate to upload internal documents such as rough sketches and calibration plans into the software. External documents such as client drawings shall be clearly categorized to include separately in your reports to comply with accreditation standards. 8. Post Test Completion
After everything is tested, your software should prompt the technician to inform your client about the test completion and any outcome (such as any markedup discontinuities) and then obtain client’s signature to indicate the testing is completed as per their requirements. Additionally, the UI Can include other administration and accounting related fields. 9. Test Record and Report
As all test data will be captured as per your procedure requirements in a process controlled UI, your system can then auto-generate a report complying with the standard, eliminating transcription errors. The software shall be configurable to produce reports as per predefined parameters to comply the requirements of the test method standard. Using the standard template, the software should be configurable to produce reports as per each client specific requirements rather than enforcing one size for all.
To assist your clients requesting tester’s qualification, the UI shall be pre-configured to auto-include tester’s certificate along with the report to ensure all items as per the client specific procedure are completed via the process control. The software shall auto-include testers signature as per pre-defined requirements of individual standards (such as ISO standards). Signatures of the signatory shall be tagged to deter bad actors from copying signature to produce a fraudulent report. Reports shall include unique QR codes for live supply chain validation. The software shall track revision controls about who altered data, when, and why. The revision notes shall be provided to the clients along with reports.
As your procedure will be software driven, you can transmit data electronically via API to your client having UID’s for each field, in the form of JSON objects or other client specified formats (such as DICONDE or HDF). Additionally, the digital data can also be shared with any external L3 or experts anywhere in the world for analysis (including PAUT, TOFD or DR files).
Conclusion
The technology to achieve this level of precision has been active and continuously being enhanced by OMS Software since 2009. By embracing digital process control, NDT facilities have protected their field personnel, delivered unmatched value to their end clients, and raised the standard of NDT in the industry. 34
The software driven procedures have:
• Eliminated errors, NCRs and rework for testers and
companies, thus increased quality and efficiency by reducing costs for all.
• Auto-produced correct reports every time due to the
prompting of pre-configured standardised data.
• Digitally communicated revised procedures and
essential parameters via UI to the testers.
• Facilitated test repeatability and reproducibility after
acceptable or undetected discontinuities were concern due to the report (or digital data transfer) containing standard's terminologies.
• Assisted L3's to analyse field data remotely,
immediately after the test data acquisition.
For any other explanation or comments about this article or for a complimentary advice to improve your current system, feel free to contact the author. About the Author: Pranay Wadyalkar Managing Director, OMS Software
Pranay Wadyalkar is a Chartered Engineer, CMatP, Metallurgist, AICIP, AINDT L3 in ET, UT, RT, MT, PT, working in laboratories for 32years. Currently, as the MD at OMS Software, a digital automation company providing business management platform and LIMS. Prior to OMS, Pranay founded LMATS providing services in the field of NDT, inspection, metallurgy, mechanical and chemical testing. Pranay is on the NATA’s NDT Advisory Committee, Steel Association Board, Australian delegate on the ICNDT, APFNDT and NDE4.0SIG. Pranay was the AINDT President from 2014-2016, and a director (2009-2017).
About the Author: Pranay Wadyalkar
Managing Director, OMS Software Pranay Wadyalkar is a Chartered Engineer, CMatP, Metallurgist, AICIP, AINDT L3 in ET, UT, RT, MT, PT, working in laboratories for 32years. Currently, as the MD at OMS Software, a digital automation company providing business management platform and LIMS.
Prior to OMS, Pranay founded LMATS providing services in the field of NDT, inspection, metallurgy, mechanical and chemical testing. Pranay is on the NATA’s NDT Advisory Committee, Steel Association Board, Australian delegate on the ICNDT, APFNDT and NDE4.0SIG. Pranay was the AINDT President from 2014-2016, and a director (2009-2017).
Industrial Eye September/October 2026
TECHNICAL ARTICLE
Impedance Spectroscopy of B40 Concrete During Hydration for Non-Destructive Strength Prediction This study investigates electrical capacitance and resistivity of B40 concrete as non-destructive strength predictors. ANATOLII M. ANTONENKO DEPARTMENT OF PHYSICS, DNIPRO NATIONAL UNIVERSITY, DNIPRO, UKRAINE;
Capacitance and resistance were measured at 100 Hz–10 kHz; resistivity was monitored over 60 days using Fe:Fe, Fe:Al and Al:Al electrode pairs. Reference strength was obtained by destructive compression testing of cubes. Capacitance exhibits strong frequency dispersion and a non-monotonic dependence on strength, with a maximum at 8–10 MPa, limiting its direct use. Resistance and resistivity increase monotonically with strength and curing time (R² > 0.98), correlating well with the reference strength curve (1.4 MPa at 6 h, 23.5 MPa at 72 h, 42.4 MPa at 28 days). Electrode material significantly affects resistivity; Fe:Fe electrodes are recommended for stable monitoring. The original piecewise model is analysed and two improved continuous models are proposed. Comparison shows that a power-law resistance model and a continuous hybrid model reduce mean absolute error to approximately 0.6–0.7 MPa over the range P = 5–33 MPa. One-time calibration enables continuous on-site monitoring and timely formwork removal.
Reference strength values obtained by standard cube compression tests are used as the ground truth for correlation analysis. In addition, the original prediction model is critically examined and two improved continuous models are developed and compared.
Materials and Methods 2.1 Materials
A B40 concrete mix was used as the test material. Measurements were performed in a specially designed measurement cell filled with the curing concrete. The mix design (Table 1) employs CEM I 52.5R cement with a water/cement ratio of 0.56. The expected 28-day strength of the mix is not less than 43 MPa. Table 1. B40 concrete mix design
Introduction
Monitoring the strength development of concrete during early hydration is critical for construction quality control. Traditional methods based on testing control specimens are time-consuming and cannot provide real-time information about in-situ concrete. Electrical impedance-based methods have attracted increasing attention as potential non-destructive techniques for monitoring concrete hydration and strength development [1–3]. The electrical properties of concrete depend on ionic mobility in the pore solution, moisture content, porosity and temperature. During hydration these parameters change significantly, affecting measured electrical parameters including capacitance (C), resistance (R) and their frequency dependencies.
However, the interpretation of impedance data is complicated by the heterogeneous nature of concrete and electrochemical processes at the electrode–concrete interface [4]. This study aims to systematically analyse the dependencies of capacitance and electrical resistivity of B40 concrete on concrete strength and curing time, and to evaluate the influence of electrode material on measurement reliability for strength prediction. Industrial Eye September/October 2026
2.2 Capacitance and Resistance Measurement Capacitance was measured at four frequencies: 100 Hz, 120 Hz, 1 kHz and 10 kHz. Active resistance of the cell was measured under alternating current at frequencies ranging from 0.1 kHz to 10 kHz. The concrete strength (P) increased from 0 to approximately 33 MPa as hydration progressed. 2.3 Electrical Resistivity Measurement
Electrical resistivity (ρ,Ω·m) was measured over 60 days of curing using three electrode pairs: p1 – Fe–Fe (steel–steel), p2 – Fe–Al (steel–aluminium) and p3 – Al–Al (aluminium–aluminium). 2.4 Reference Strength Measurement
Compressive strength of concrete cubes was determined by the laboratory approach. Five cube specimens were tested at each curing age. The average strength was calculated as the arithmetic mean of valid measurements. The test schedule included ages from
35
TECHNICAL ARTICLE
6 h to 28 days (673 h). Results are presented in Table 2. Table 2. Compressive strength of concrete cubes versus curing time
the measured value reflects mainly the geometric capacitance.
The low-frequency curves (100 Hz, 120 Hz) exhibit a clear maximum at concrete strength of 8–10 MPa, corresponding to the curing interval between 12 h and 24 h. The subsequent decrease is caused by water binding and pore refinement. This non-monotonic behaviour prevents unambiguous strength prediction from absolute capacitance values alone.
2.5 Data Processing Experimental data were fitted using third-order polynomials (for capacitance) and linear or powerlaw functions (for resistance and resistivity), with the coefficient of determination R² evaluated.
Results and Discussion
3.1 Reference Strength Development Figure 1 presents the reference compressive strength of concrete cubes versus curing time. The strength curve exhibits a characteristic two-stage behaviour: rapid early-age gain (1.4 MPa at 6 h, 8.8 MPa at 12 h, 16.5 MPa at 24 h and 23.5 MPa at 72 h) followed by a gradual long-term development (33.1 MPa at 7 days, 38.8 MPa at 14 days and 42.4 MPa at 28 days). This behaviour is typical for B40 concrete and reflects the progression of cement hydration: the initial rapid stage corresponds to the formation of ettringite and initial C–S–H, while the later stage is governed by slower diffusioncontrolled hydration [1, 5]. The 28-day strength of 42.4 MPa confirms that the mix satisfies the B40 class requirement.
Figure 2. Capacitance (C) versus concrete strength (P) for four measurement frequencies (100 Hz, 120 Hz, 1 kHz, 10 kHz) with polynomial approximations
3.3 Active Resistance versus Concrete Strength Figure 3 shows active resistance versus concrete strength for frequencies from 0.1 kHz to10 kHz. Unlike capacitance, active resistance increases monotonically with concrete strength. Linear fitting yields R² = 0.9857. All frequency series lie close to each other, indicating that ionic conduction in the pore solution dominates the active resistance in this frequency range [2, 3]. These results demonstrate that active resistance is a more reliable and simpler parameter for strength prediction than capacitance.
Figure 1. Reference compressive strength of concrete cubes versus
curing time (destructive testing, average of up to five specimens per age)
3.2 Capacitance versus Concrete Strength and Frequency Figure 2 presents capacitance versus concrete strength for the four frequencies. A pronounced frequency dispersion is observed: capacitance decreases from approximately 40–60 µF at 100 Hz to 5–15 µF at 10 kHz. This is attributed to interfacial (Maxwell–Wagner–Sillars) polarisation [4, 6]. At low frequencies ions and dipolar water molecules accumulate at phase boundaries, creating significant pseudo-capacitance. At high frequencies polarisation cannot develop and
36
Figure 3. Averaged active resistance (R) versus concrete strength (P) for frequencies from 0.1 kHz to 10 kHz with linear approximation (R² = 0.9857)
Industrial Eye September/October 2026
TECHNICAL ARTICLE
3.4 Effect of Electrode Material on Electrical Resistivity
4.2 Improved Model A – Continuous Power-Law Resistance Model
Figure 4 presents electrical resistivity evolution over 60 days for the three electrode pairs. All curves show monotonic increase with curing time, reflecting water binding and reduced ionic conduction. Linear fits for Fe–Fe and Al–Al pairs yield R² > 0.98. The electrode material significantly affects measured resistivity: Fe–Fe gives the lowest and most stable values (~155 ·m at 60 days), while mixed Fe–Al and Al–Al pairs produce higher values and greater scatter due to passivation and galvanic effects [4]. Homogeneous Fe–Fe electrodes are therefore recommended for long-term monitoring.
Because resistance exhibits a clear monotonic and nearly linear rise with strength, a simple continuous powerlaw relation can be fitted directly to the normalised resistance data: (3) Least-squares fitting on the same data set yields a ~ 11.8 and b ~ 1.05 (R² ~ 0.989). The slight superlinearity accounts for the progressive pore refinement that accelerates resistance growth at higher strengths. Temperature compensation remains the same as in the original model. This formulation eliminates the need for any capacitance measurement and is therefore simpler for field use. 4.3 Improved Model B – Continuous Hybrid Model
A continuous hybrid model retains the information contained in high-frequency capacitance while removing the discontinuities of the piecewise factor. The capacitance correction is expressed as a smooth sigmoid function of the normalised capacitance ratio x = C10k/C0: (4)
Figure 4. Electrical resistivity evolution over 60 days for Fe–Fe, Fe–Al and
(5)
Al–Al electrode pairs
Strength Prediction Models
4.1 Analysis of the Original Piecewise Model The original piecewise model uses normalised resistance as the primary predictor and a piecewise correction factor kC derived from high-frequency capacitance: (1)
(2) A discrete correction kC (taking values 1.30, 1.15, 1.00, 0.92 or 0.96 according to the ratio C10k/C0) and a linear temperature factor kT = 1 + 0.025·(20 T) are then applied. Validation against the experimental data set gave a mean absolute error (MAE) of
The sigmoid was calibrated so that its plateau values reproduce the original discrete levels while providing a continuous transition. The resulting model preserves the physical insight of the original approach (resistance as primary predictor, capacitance as stage indicator) yet avoids abrupt jumps. 4.4 Comparison of Model Performance
Table 3 summarises the predictive performance of the three models on the same evaluation points used for the original model (P = 8, 16, 24 and 33 MPa). Mean absolute error and
Table 3. Comparison of prediction models (evaluation points)
approximately 0.9 MPa and a maximum error of 2.3 MPa (~7 %) over the range P = 5–33 MPa. While the model is practical, the stepwise nature of kC introduces discontinuities and requires careful determination of the capacitance ratio thresholds.
Industrial Eye September/October 2026
37
TECHNICAL ARTICLE
Both improved models reduce the mean absolute error relative to the original piecewise formulation. Model A (power-law) achieves the lowest MAE (0.33 MPa) and is the simplest to implement on site, requiring only resistance and temperature measurements after a single initial calibration of R0. Model B retains the physical interpretation of the capacitance stage indicator and still improves upon the original discontinuous correction. For practical construction monitoring the power-law Model A is therefore recommended, while Model B may be preferred when high-frequency capacitance data are already being collected for research purposes. 4.5 Practical Implementation and Limitations
On a typical construction site a single concrete grade is supplied by the same producer under controlled conditions. Consequently a one-time calibration performed on the first batch is sufficient for subsequent batches. The measurement cell containing mild-steel electrodes (identical in material to the reinforcing bars) can be embedded directly into a structural element. Once connected to a portable impedance analyser, real-time readings of
R/R0 (and optionally C10k/C0) allow the current strength to be calculated. This capability supports timely formwork removal, reducing rental and labour costs.
References
1. McCarter W. J., Chrisp T. M. and Starrs G., ‘The use of electrical impedance measurements to monitor the early hydration of cement’, Journal of Materials Science, Vol 35, No 15, pp 3817–3825, 2000.
2. Princigallo A., van Breugel K. and Levita G., ‘Influence of the aggregate on the electrical conductivity of Portland cement mortars’, Cement and Concrete Research, Vol 33, No 11, pp 1755–1763, 2003.
3. Whittington H. W., McCarter J. and Forde M. C., ‘The conduction of electricity through concrete’, Magazine of Concrete Research, Vol 33, No 114, pp 48–60, 1981.
4. Bard A. J. and Faulkner L. R., Electrochemical Methods: Fundamentals and Applications, 2nd ed., John Wiley & Sons, 2001. 5. McCarter W. J., ‘The a.c. impedance response of concrete during early hydration’, Journal of Materials Science, Vol 31, pp 6285–6292, 1996.
6. McCarter W. J. and Garvin S., ‘Dependence of electrical impedance of cement-based materials on their moisture condition’, Journal of Physics D: Applied Physics, Vol 22, pp 1773–1776, 1989.
The models are applicable to B40 concrete with Fe–Fe electrodes in the strength range approximately 5–33 MPa and for temperatures 15–30 °C. For other concrete grades or mix compositions recalibration of the coefficients is required. The measurement cell must remain sealed to prevent moisture loss.
Conclusions
1. Reference compressive strength testing confirmed that the B40 mix reaches 1.4 MPa at 6 h, 23.5 MPa at 72 h and 42.4 MPa at 28 days, with a characteristic two-stage hydration behaviour. 2. Electrical capacitance exhibits strong frequency dispersion and a non-monotonic dependence on concrete strength with a maximum at 8–10 MPa, limiting its direct use for strength prediction.
3. Active resistance and electrical resistivity increase monotonically with concrete strength and curing time (R² > 0.98), making them preferred parameters for non-destructive strength monitoring. Fe–Fe electrodes provide the most stable resistivity readings. 4. The original piecewise prediction model was analysed and two continuous improved models were developed. A simple power-law resistance model (Model A) reduces mean absolute error to approximately 0.33 MPa, while a continuous hybrid model (Model B) yields MAE 0.43 MPa. Both outperform the original discontinuous formulation. One-time calibration enables continuous on-site strength monitoring and optimised formwork removal.
38
Industrial Eye September/October 2026
TECHNICAL ARTICLE
A New Methodology to Predict Moisture-Induced Stiffness Degradation in Bio-based Composite Sandwich Structures using Acoustic Emission Wave Velocity This study investigates moisture absorption behavior and moisture-induced stiffness degradation in several bio-based composite sandwich structures, through water immersion tests, AE wave velocity measurements and 4-poing bending tests. YUAN WU1, PASCAL CASARI1, SYLVAIN FRÉOUR1, MARIANNE PERRIN2, MARIE-LAETITIA PASTOR2, XIAOJING GONG2 1: NANTES UNIVERSITÉ, ECOLE CENTRALE NANTES, CNRS, INSTITUT DE RECHERCHE EN GÉNIE CIVIL ET MÉCANIQUE (GEM), UMR 6183, SAINT-NAZAIRE, FRANCE 58 RUE MICHEL ANGE, F- 44600 SAINT-NAZAIRE, FRANCE E-MAIL: YUAN.WU@UNIV-NANTES.FR 2: UNIVERSITÉ TOULOUSE, UTTOP, IMT MINES ALBI, INSA TOULOUSE, ISAE-SUPAERO, CNRS, ICA, TARBES, FRANCE E-MAIL: MARIANNE.PERRIN@IUT-TARBES.FR
In this work, a new method for predicting stiffness degradation using AE wave velocity is demonstrated effective for GFRP (Glass-Fiber-Reinforced-Polymer)Okoume, GFRP-Pine, GFRP-Flax, and GFRP-Balsa composite sandwich structures. It is shown that AE wave velocity could decrease as a function of Moisture Content (MC), with higher MC leading to more pronounced reductions in AE wave velocity and structural stiffness. Additionally, for each core material, two distinct dog-bone specimen shapes were examined, and the results exhibited nearly identical AE wave velocity and bending stiffness. A significant stiffness degradation was observed in GFRP-Balsa specimens, with a reduction of 20 % at a MC of 140 %. In contrast, for the GFRP-Okoume, GFRP-Pine and GFRP-Flax specimens, both AE wave velocity and bending stiffness remained nearly unchanged at MCs of 17 %, 19 % and 7 %, respectively. These findings provide fundamental support for the application of AE methods to structure health monitoring and damage localization in composite structures exposed to harsh humid environments.
Introduction
To address the increasingly severe climate change on Earth, various industrial sectors including aeronautical and marine structure production are endeavoring to develop innovative solutions, through the development of novel bio-based composite sandwich structures [12] as potential alternatives to traditional Carbon- and Glass-Fiber-Reinforced-Polymer (GFRP) laminates. However, composite structures made of natural-fiberbased cores, such as wood and flax fibers, inherently Industrial Eye September/October 2026
exhibit pronounced hydrophilic behavior [2] compared to synthetic-fiber-based composites. As a result, their higher moisture absorption capacity could lead to severe and irreversible degradation of mechanical performance. Moisture-induced stiffness degradation thus remains a major concern for the long-term durability of bio-based composite structures, particularly due to hygroscopic swelling effects and the associated internal damage evolution.
To assess the structural integrity of composite materials, the Acoustic Emission (AE) technique [3-4] has been widely employed as a non-destructive method to identify and localize microscopic damages. Nevertheless, accurate localization [4] of different damage modes in composite structures remains a significant challenge for the wide application of AE methods. To address this limitation, further investigation of AE wave propagation characteristics [5-6], including wave velocity and attenuation, is required to enhance the accuracy of damage localization. Based on the plate wave theory, it was demonstrated [5] that AE wave velocity in conventional synthetic composite structures is primarily governed by elastic modulus of the structure, material density, and Poisson’s ratio. Consequently, the reduction in structural stiffness is expected to be reflected by a decrease in AE wave velocity. Based on the correlation between Moisture Content (MC), AE wave velocity and elastic modulus, moisture-induced stiffness degradation [6] can be predicted simply and efficiently. However, the accuracy of such predictions may be influenced by multiple factors, including intrinsic material properties, structural dimensions, hygroscopic swelling effects, and possible variations in Poisson’s ratio. Particularly, natural-fiber-based composites exhibit higher dimensional swelling under long-term water immersion. Therefore, further validation of this approach is required to cover a wide range of bio-based composite materials and structural configurations [7-8]. In this work, water immersion tests, AE wave velocity measurement and 4-poing bending tests were conducted to investigate moisture-induced stiffness degradation in four different bio-based composite
39
TECHNICAL ARTICLE
sandwich structures. The AE-based method previously proposed [6] for predicting stiffness degradation in GFRP-Balsa specimens was further validated and extended to other natural-fiber-based composite sandwich structures, with different core materials and structural shapes.
Materials and experimental methods 2.1. Materials and specimens
Based on our previous studies [5-6], AE wave velocity has been proven to be an effective indicator for the non-destructive testing of moisture-induced stiffness degradation in composite structures. However, this novel method needs to be further validated in different materials and structural configurations. Accordingly, this work investigates bio-based composite sandwich specimens with the same skin mode of Glass-FiberReinforced-Polymer laminates (GFRP) and four different natural-fiber-based cores: namely GFRP-Okoume, GFRP-Pine, GFRP-Flax, and GFRP-Balsa. As illustrated in Fig. 1, all specimens have a length of 300 mm and a width of 80 mm. The three types of the specimens in Fig. 1(a) have a similar thickness of approximately 4 mm, whereas the thickness of GFRP-Balsa specimens is set to 10 mm thickness. To study the effect of structure dimensions on moisture absorption behavior and stiffness degradation, two groups of structural shapes have been fabricated: dog-bone specimens (Group 1) and double dog-bone specimens (Group 2). All GFRP skins of these composite sandwich specimens were manufactured using three-layer woven balanced fabric/ epoxy laminates (Sicomin E glass fiber twill 3190, 190 g/m², with a fiber volume fraction of 50 %).
2.2. Moisture absorption tests monitored by AE wave velocity According to ISO 12571 and ASTM D5229 [6], three specimens of each material in each group were immersed into water at room temperature until mass stabilization was achieved. On the first day, the specimen mass was measured twice a day, because the water absorption rate was typically higher during the initial stage of immersion. Subsequently, mass measurements were conducted every 24 hours. Finally, the Moisture Content (MC) in each specimen at time t, denoted as 𝑐(𝑡), which is water weight fraction, i.e. the ratio of the mass of absorbed moisture to the initial mass of the specimen, can be defined by Eq. 1: (Eq. 1) which is defined as the dry mass in this work [6], mw being the mass of wet specimen at time t.
Throughout the entire moisture absorption process, active Hsu-Nielsen (pencil lead break) tests were regularly performed along the specimen length direction (0°, Direction X) (see Fig. 2) to monitor the moistureinduced decrease in AE wave velocity, which, in the present work, is considered to reflect the corresponding stiffness degradation in the same direction. Distance between sensors S1 and S2 was 100 mm, and the distance between sensor S1 and the source was 50 mm. AE wave velocity can then be calculated using Eq. 2: (Eq. 2) where ∆𝑡 is the difference between the arrival times of the maximum amplitude at each sensor, and ∆𝑑 is the distance between the two sensors
(a) Specimens with the same thickness of 4 mm
Fig. 2. AE wave velocity testing to monitor stiffness degradation of composite structures.
Theoretically [5-6], the elastic modulus in the 0° direction of the dry specimen can be calculated based on Eq. 3: (b) 10 mm thick GFRP-balsa specimens
Fig. 1. Studied bio-based composite specimens: GFRPOkoume, GFRP-Pine, GFRP-Flax, GFRP-Balsa.
40
(Eq. 3)
Industrial Eye September/October 2026
TECHNICAL ARTICLE where 𝜌𝑖 is the density of the dry specimen, 𝑣𝑖(0°) is the AE wave velocity of the dry specimen in the 0° direction, and φi(0°) is Poisson’s ratio of the dry specimen in the 0° direction. Next, assuming that the influence of moisture on Poisson’s ratio can be neglected [3, 5], the elastic modulus in the 0° direction of the wet specimen can be predicted using Eq. 4: (Eq. 4)
Subsequently, if the influence of moisture on the structural volume can be negligible [6], Eq. 5 can be obtained: (Eq. 5)
where 𝑟 = 𝑣𝑤(0°) 𝑣𝑖(0°) is the ratio of the AE wave velocity in the wet specimen to that in the dry specimen. 𝑐(𝑡) is the Moisture Content (MC) in Eq. 1.
Eq. 5 has been validated on triple dog-bone GFRPbalsa specimens in [6], as their hygroscopic swelling is approximately 1 % [2], which can be neglected. However, effects of hygroscopic swelling should be taken into account when the volume change is more significant, particularly for natural plant fibres. Then, Eq. 5 can be corrected by considering the volume change, as shown in Eq. 6: (Eq. 6a)
(Eq. 6b) where 𝑉𝑖(𝑡) and 𝑉𝑤(𝑡) are the structural volume of the dry and wet specimens, respectively. 𝛼 = 𝑉𝑖(𝑡) 𝑉𝑤(𝑡) is the ratio of 𝑉𝑖(𝑡) to 𝑉𝑤(𝑡).
Fig. 3. 4-point bending test.
Results and discussion
3.1. Moisture absorption behavior of the studied bio-based composite structures Fig. 4 presents the average moisture absorption curves of the GFRP-Balsa, GFRP-Okoume, GFRP-Pine, and GFRP-Flax specimens. First, it is noteworthy that the repeatability between the two groups for each material is satisfactory with a maximum standard deviation of ± 1.5 % for the GFRP-Okoume specimens. At the time of measurement, the mass equilibrium had not been achieved, and the immersion tests were still ongoing. After 600 days of immersion, the average moisture content of the GFRP-Balsa specimens reached 140 %, with a standard deviation of ± 14 %. After 300 days, the average moisture content values of the GFRPOkoume, GFRP-Pine, and GFRP-Flax specimens were approximately 17 %, 19 % and 7 %, respectively, with corresponding standard deviations of ± 4 %, ± 3 % and ± 2 %.
These results indicates that the two wood-core sandwich structures (GFRP-Okoume and GFRP-Pine) exhibit similar moisture absorption behavior, while the water absorption in GFRP-Balsa structure is significantly more important than the other bio-based composite materials. In contrast, the GFRP-Flax structures demonstrate excellent hygroscopic performance.
2.3. 4-point bending tests to evaluate stiffness degradation
Additionally, 4-point bending tests (see Fig. 3) were conducted on all dry and wet specimens to validate the moisture-induced stiffness degradation predicted from the AE wave velocity decrease. All tests were controlled at a displacement rate of 10 mm/min and stopped at 3 mm to ensure that the specimen remained undamaged.
(a) Comparison of GFRP-Balsa specimens in Groups 1 and 2
Industrial Eye September/October 2026
41
TECHNICAL ARTICLE
(b) Average curves of GFRP-Okoume, GFRP-Pine and GFRP-Flax specimens in Groups 1 and 2 Fig. 4. Moisture diffusion kinetics of bio-based composite structures.
(a) AE wave velocity decrease in all specimens
3.2. Prediction of moisture-induced stiffness degradation using AE wave velocity
Fig. 5 illustrates the decrease of AE wave velocity in various bio-based composite structures. In this work, the average measured wave velocity of all specimens in the two groups is compared in Fig. 5(a), since no significant difference was observed between the specimens with different geometrical shapes. In Fig. 5(b), it is shown that the AE wave velocity in GFRP-Pine, GFRP-Okoume and GFRP-Flax specimens exhibited only a small decrease of less than 10 %, so their stiffness did not decrease significantly even after 300 days of water immersion. This is why only the results of the GFRPBalsa and GFRP-Okoume specimens will be discussed herein. It can be seen in Tab. 1 that a significant decrease of 44 % in AE wave velocity was observed for the GFRP-Balsa specimens, corresponding to an approximately 25 % reduction in the predicted stiffness. However, there is no moisture-induced stiffness degradation predicted by Eq. 5 for the GFRP-Okoume specimens (to see Tab. 2).
In fact, the AE wave velocity in a sandwich structure is mainly dominated by the elastic modulus of the skin, the density and thickness of the skin and core [6]. Because the measured hygroscopic swelling of the GFRPOkoume specimens in the thickness direction was 3 %, a correction coefficient α = Vi(t) , which is 0.97 in this work, could be introduced into Eq. 6. This consideration introduces just 1% stiffness degradation, so small to be negligible after 300 days of water immersion. This will be demonstrated by 4-point bending tests.
(b) AE wave velocity decrease in specimens with lower MC
Fig. 5. AE wave velocity decrease in different bio-based composite structures.
Tab. 1. Predicted moisture-induced stiffness degradation in GFRP-Balsa specimens.
Tab. 2. Predicted moisture-induced stiffness degradation in GFRP-Okoume specimens.
42
Industrial Eye September/October 2026
TECHNICAL ARTICLE
3.3. Validation of stiffness degradation through 4-point bending tests Fig. 6 illustrates the average Force-Displacement curves of the GFRP-Balsa and GFRP-Okoume specimens in the two groups at different MCs, since the two structural shapes exhibited nearly identical bending stiffness (see Tab. 3 and Tab. 4). As presented in Fig. 7, a notable stiffness degradation was observed in the GFRP-Balsa specimens, with a reduction of 20 % at a MC of 140 %. The discrepancy between the predicted and tested stiffness values was approximately 6 %, and remains close to the confidence intervals corresponding to the estimated uncertainties. In order to obtain a better agreement, it would be necessary to account for the volume change due to the hygroscopic swelling to improve the accuracy of the predicted values achieved through Eq. 6.
(a) GFRP-Balsa specimens
In contrast, for the GFRP-Okoume specimens, the bending stiffness remained nearly unchanged at an MC of 17 %. This observation is consistent with the predicted stiffness (see Fig. 7(b)), demonstrating that this new AE-based method for predicting moistureinduced stiffness degradation is effective and accurate for bio-based composite structures.
(b) GFRP-Okoume specimens
Fig. 7. Comparison of the predicted and measured stiffness.
(a) GFRP-Balsa specimens(b) GFRP-Okoume specimens
Tab. 3. Measured moisture-induced stiffness degradation in GFRP-Balsa specimens.
Fig. 6. Average Force-Displacement curves of GFRPBalsa and GFRP-Okoume specimens.
Tab. 4. Measured moisture-induced stiffness degradation in GFRP-Okoume specimens.
(a) GFRP-Balsa specimens(b) GFRP-Okoume specimens Fig. 7. Comparison of the predicted and measured stiffness.
Industrial Eye September/October 2026
43
TECHNICAL ARTICLE
Conclusions
This study demonstrates a new AE-based method for predicting moisture-induced stiffness degradation in bio-based composite structures, through investigating sandwich specimens made from four different core materials with two structural shapes: GFRP-Okoume, GFRP-Pine, GFRP-Flax, and GFRP-Balsa. It has been proven that AE wave velocity would decrease as a function of MC, and higher MC could cause more pronounced reductions in AE wave velocity and structural stiffness. Therefore, AE wave velocity can be applicable to evaluate structural stiffness degradation in composite structures for industrial applications in harsh humid environments, enabling efficient, non-destructive assessment while saving time and costs associated to the realization of conventional mechanical tests. Meanwhile, the proposed AE wave velocity calculation method, incorporating the effect of moisture content, provides a promising basis for accurate damage localization in composite structures under loading.
Nevertheless, this novel method needs to be further validated across a wide range of composite materials and corrected by incorporating the more accurate hygroscopic swelling measurements in all principal directions of anisotropic structures. Acknowledgements
The authors would like to thank their colleagues at the GeM laboratory for their technical support, especially the Master’s intern Chouaib Difallah, who helped verify the feasibility of the related tests during his internship in 2025.
44
References
[1] H. Yu, L. Yao, Y. Ma, Z. Hou, J. Tang, Y. Wang, Y. Ni « The Moisture Diffusion Equation for Moisture Absorption of Multiphase Symmetrical Sandwich Structures », Mathematics Vol. 10, pp. 2669, 2022. [2] Y. Wu, P. Casari, J. Fajoui, S. Fréour, M. Bouziane « Characterization of cyclic hygroscopic swelling and shrinkage behavior of balsa wood and GFRPbalsa sandwich structures », in: 14th International Conference on Sandwich Structures (ICSS-14), Genova, Italy, 16–18 June 2025.
[3] N. Ghadarah, D. Ayre « A review on acoustic emission testing for structural health monitoring of polymer-based composites », Sensors Vol. 23(15), pp. 6945, 2023. [4] T. Kundu, H. Nakatani, N. Takeda « Acoustic source localization in anisotropic plates », Ultrasonics Vol. 52(6), pp. 740-746, 2012. [5] Y. Wu, M. Perrin, M. L. Pastor, P. Casari, X. Gong « On the determination of acoustic emission wave propagation velocity in composite sandwich structures », Composite Structures Vol. 259, pp. 113231, 2021.
[6] Y. Wu, M. L. Pastor, M. Perrin, P. Casari, X. Gong « A new methodology to predict moisture effects on mechanical behaviors of GFRP-balsa sandwich by acoustic emission and infrared thermography », Composite Structures Vol. 287, pp. 115342, 2022. [7] N. Osa-Uwagboe, V. V. Silberschmidt, K. P. Baxevanakis, E. Demirci « Effects of moisture absorption on penetration performance of FRP sandwich structures », Composite Structures Vol. 344, pp. 118319, 2024.
[8] A. Célino, S. Fréour, F. Jacquemin, P. Casari « The hygroscopic behavior of plant fibers: a review », Frontiers in chemistry Vol. 1, pp. 43, 2014.
Industrial Eye September/October 2026
TECHNICAL ARTICLE
CONNECT, LEARN & LEAD GET AINDT CERTIFIED TODAY AINDT Certification demonstrates that you have the necessary knowledge and skills to carry out inspections, testing, and analysis to detect flaws or defects in materials and structures without causing damage. As the primary Certification Body in Australia for the NDT and CM industry, our certification is recognised, respected, and streamlined. Independent verification of your competence Widely recognised and respected across the Australian industry Boosts employability and career progression Demonstrates commitment to safety, quality and compliance Builds confidence with employers, clients and auditors Reduces risk, rework and downtime Portable credential across sectors
LEARN MORE >>> Industrial Eye September/October 2026
aindt.com.au
45
INDUSTRY NEWS
NDT World Event Calendar NDE for Safety 2026
11 to 13 November 2026 | Společenský dům, Františkovy Lázně The NDE for Safety conference will cover all topics related to non-destructive testing and evaluation of materials and structures in all areas of technical activities. It is an opportunity to come together with like-minded professionals interested in NDT research and development, as well as practice, standardisation and application of NDT methods. Manufacturers and suppliers of NDT instruments and services are invited to present their products and innovations.
For further information, visit: cndt.cz/en/conference
NDE 2026
15 to 17 November 2026 | Hyderbad, India This premier event with bring together over 2,000 professionals, researchers, and industry leaders to exchange transformative ideas, innovations, and advancements in the ever-evolving domain of NDE. These breakthroughs will be demonstrated by an exhibition featuring over 100 companies, showcasing best-in-class achievements. With the theme Innovation for Strategic and Economic Excellence, sessions will cover critical sectors like defence, aerospace, renewables, oil and gas, manufacturing and more. For further information, visit: isntnde.in
8th Malaysia International NDT Conference and Exhibition (MINDTCE) 17 to 18 November 2026 | Selangor, Malaysia
The 8TH MINDTCE is the definitive biennial event for the NDT community in southeast Asia. Organised by the MSNT, the event bridges the gap between academic research and industrial application. It brings together scholars, engineers and key decision-makers to explore the technologies that ensure the safety and integrity of our world’s infrastructure. It will cover topics like NDT methods and techniques, NDT 4.0 and digital transformation, safety, compliance, education and professional development, and more. For further information, visit: mindtce.com.my
8th African Conference on Non-Destructive Testing (ACNDT) 18 to 19 November 2026 | Tunis, Tunisia
Organised by the African Federation for Non-Destructive Testing (AFNDT), ACNDT 2026 will bring together experts, researchers, engineers, industry professionals, and decision-makers from around the world to share the
46
latest scientific, technological, and industrial advances in the field of non-destructive testing. The conference offers a unique platform for knowledge exchange, development, networking, partnerships, and the promotion of innovation. For further information, visit: sapri.tn/acndt-2026
NDTMA 2027 Annual Conference
23-25 February 2027 | Las Vegas, USA The Non-Destructive Testing Management Association (NDTMA) brings together the industry's top decisionmakers to learn best practices, share ideas and help the NDT sector thrive. The program covers the issues that matter most, from spending and acquisitions to education, apprenticeships, certification, standards and regulation, alongside presentations on emerging technologies and trends. You'll meet the rising talent in the Young Professionals Program and celebrate this year's award winners. For further information, visit: ndtma.org
Quantitative Infrared Thermography Asia Conference (QIRT-Asia 2027)) 7 March 2027 | Singapore
The Quantitative Infrared Thermography (QIRT) conference is a biennial international event where infrared thermography specialists from industry and academia present their latest work and new developments. Since 1992, QIRT has been held around the world, building a strong tradition of excellence in thermal imaging research and applications. The 6th QIRT-Asia will take place in Singapore in 2027, bringing together researchers, engineers and industry professionals from around the world. For further information, visit: qirtasia2027.com
16th Conference on Industrial Computed Tomography 9 March 2027 | Grenoble, France
This leading annual event is a unique platform for presenting and discussing the latest developments in industrial computed tomography and its wideranging applications, from material characterisation and dimensional metrology to automated inspection and advanced reconstruction algorithms. The program traditionally includes keynote lectures, dedicated industry sessions, and peer-reviewed scientific research presented in oral and poster sessions. For further information, visit: ict2027.inviteo.fr
Industrial Eye September/October 2026
PRODUCTS & SERVICES
Condition Monitoring Group CM Group is a group of businesses providing specialist services, training and products to the industrial and commercial sectors.
CM Solutions is a specialist provider of industrial maintenance, diagnostic services and engineering support for complex machinery and plant assets across Australia and internationally. Our core objective is to help clients improve reliability, minimise unplanned downtime and maintain safe, stable, and efficient operations. CM Institute delivers industry-focused training in Vibration Analysis, Infrared Thermography, Precision Alignment and other condition monitoring disciplines, combining technical knowledge with practical,
OMS Engineering
OMS Engineering is a NATAaccredited Non-Destructive Testing (NDT) services provider, delivering reliable inspection solutions to the mining, manufacturing, and fabrication industries. Their experienced and qualified technical team is committed to providing high-quality workmanship, professional service and dependable inspection outcomes. They provide a comprehensive range of NDT services to support the integrity, safety and reliability of critical plant, equipment and fabricated components. Their capabilities include Magnetic Particle Testing (MT), Liquid Penetrant Testing (PT), Ultrasonic Testing (UT) Eddy Current Testing (ET) and Visual Inspection.
Russell Fraser Sales
NDT Equipment, Inspection Solutions and Technical Support
Russell Fraser Sales (RFS) is a trusted Australian supplier of Non-Destructive Testing (NDT), inspection and testing equipment, supporting professionals across industries including mining, oil and gas, manufacturing, engineering, defence, infrastructure and asset maintenance. With decades of industry experience, RFS supplies a comprehensive range of NDT equipment, consumables and inspection solutions for applications including Ultrasonic Testing (UT), Magnetic Particle Testing (MT), Dye Penetrant Testing (PT), Visual Inspection, Eddy Current Testing and other specialised inspection requirements. We are proud to partner with leading international
Industrial Eye September/October 2026
real-world application through classroom and onsite training.
CM Products supplies condition monitoring tools and test instruments designed to detect faults early, optimise maintenance and protect critical assets. Our range includes thermal and acoustic imaging systems, precision shims, automatic lubrication systems and advanced online machine monitoring platforms. Multi-sensor monitoring solutions capture, trend and analyse condition data including vibration, temperature and other key signals, providing greater visibility of equipment health. Together, CM Group connects services, training and technology to help organisations improve reliability, build capability and better understand the condition of their critical assets. For further information, visit: cm-group.au
Their inspection capabilities cover welds, forgings and castings, including the detection of surface, nearsurface and subsurface discontinuities. Ultrasonic services include inspection of welded components, forgings and castings, ultrasonic thickness measurement, lamination scanning of rolled plate, and in-situ examination of shafts, pins and bolts.
With a strong focus on quality, safety, responsiveness and technical expertise, OMS Engineering works closely with clients to provide practical NDT solutions suited to both workshop and field environments. Their goal is to help clients maintain equipment integrity, identify defects early and support safe, reliable operations. OMS Engineering – Professional NDT and Inspection Solutions You Can Rely On. For further information, visit: oms.net.au
manufacturers and brands, including Cygnus Instruments, Magnaflux, Sonatest, Phoenix Inspection Systems, GB Inspection Systems, Carestream NDT, JME, Spectro-UV and Parker Research, bringing proven inspection technologies to the Australian market.
Our product range includes ultrasonic thickness gauges, ultrasonic flaw detectors, probes and transducers, magnetic particle and penetrant inspection products, UV inspection equipment, remote visual inspection systems, eddy current equipment and a wide selection of NDT accessories and consumables. At Russell Fraser Sales, we focus on more than simply supplying equipment. Our experienced team works closely with customers to understand their inspection requirements and help identify suitable equipment and solutions for their applications. For NDT equipment, product advice or assistance selecting the right inspection solution, contact the Russell Fraser Sales team at NDT@cebeco.com.au For further information, visit: rfsales.com.au
47
PRODUCTS & SERVICES
SmartChem Industries
SmartChem Industries is your trusted partner for magnetic particle and dye penetrant requirements, with over 100 years combined experience in the manufacture and distribution of magnetic particle and dye penetrant consumables.
Established in 2012, Smartchem is 100% Australian owned and proudly manufactures in Australia with Australian resources where possible. SmartChem prides itself on service, both technical and in the delivery of our products. The SmartCheck MPI range complies with the requirements ISO-9934.2 and other relevant standards. The SmartCheck dye penetrant range has been third party type tested to ISO 3452.2 by MPA Hanover in Germany. This range now includes the SmartCheck Dye Pen Fluoro: a level three water washable and solvent removable fluorescent dye penetrant.
SRG Global Asset Care
SRG Global Asset Care is a leading provider of inspection, non-destructive testing (NDT), asset integrity, and engineering services, supporting the safe, reliable, and efficient operation of critical assets across the energy, mining, oil and gas, petrochemical, manufacturing, transport, water, and infrastructure sectors.
With a national workforce of more than 650 inspectors, technicians, engineers, metallurgists, and asset integrity specialists, we deliver comprehensive technical solutions under NATA-accredited and ISO-certified management systems. Our capabilities span conventional and advanced inspection technologies including Ultrasonic Testing (UT), Magnetic Particle Inspection (MPI), Dye Penetrant Testing (PT), Eddy Current Testing (ECT), Radiographic Testing (RT), Phased Array Ultrasonic Testing (PAUT),
Total Asset Solutions
Delivering Asset Integrity for Safer, More Reliable Infrastructure.
Total Asset Solutions is a Tasmanian-owned and operated business dedicated to helping organisations improve the safety, reliability and performance of their assets through advanced inspection and monitoring services.
Working across a range of industries, Total Asset Solutions specialises in thermographic inspections and drone-based asset inspections, providing clients with valuable insights into the condition of critical infrastructure and equipment. By identifying potential issues before they become costly failures, Total Asset Solutions helps businesses minimise downtime, reduce risk, and make informed maintenance decisions. Using advanced infrared thermal imaging technology, the team can detect hidden defects in electrical and 48
All CoC and SDS are available on the SmartChem website, which is a useful reference tool for an audit or where a copy is required in the field. SmartChem is the exclusive distributor for the Matcon range of magnets and equipment. They are also exclusive distributors for Promag UV lights and equipment.
SmartChem supplies direct and has a network of resellers throughout Australia. Please contact them for your nearest reseller on the east coast. Heatleys Safety and Industrial (heatleys.com.au) are their distributor in Western Australia, ensuring all SmartChem products available via a well-established distribution network. SmartChem’s products are now available in New Zealand, stocked in both the North and South Island through their new distributor Accurate Instruments (accurate.kiwi). For further information, visit: smartchem.com.au
TOFD, Pulsed Eddy Current Testing (PECT), Long Range Ultrasonic Testing (LRUT), EMAT, corrosion mapping, digital radiography, and specialised integrity assessment techniques.
What differentiates SRG Global Asset Care is our ability to combine inspection and asset integrity expertise with engineering capability. Beyond identifying defects and degradation mechanisms, our engineers provide fitnessfor-service assessments, remaining life evaluations, failure investigations, and practical repair and maintenance recommendations that enable informed asset management decisions.
Supported by the broader SRG Global group, we can then deliver the recommended remediation, maintenance, strengthening, specialist access, and asset preservation solutions, providing clients with a true end-to-end asset management partner and a single point of accountability throughout the asset lifecycle. For further information, visit: srgglobal.com.au
mechanical systems, solar installations, buildings, and other key assets. These inspections provide a noninvasive method of assessing asset condition while supporting improved safety and operational efficiency.
In addition, licensed drone services enable safe and effective inspections of structures and locations that may be difficult, costly, or hazardous to access using traditional methods. This approach allows for detailed visual and thermal assessments while reducing risks to personnel and minimising disruption to operations.
With a strong commitment to professionalism, innovation, and customer service, Total Asset Solutions continues to support businesses and organisations throughout Tasmania and Australia. Through the use of modern inspection technologies and practical asset management solutions, the company helps clients protect their investments and maintain reliable operations for the future. For further information, visit: totalassetsolutions.com.au Industrial Eye September/October 2026
Be Ready for What’s Next
The New OmniScan™ X4 Flaw Detector Engineered for Speed & Simplicity Advanced imaging technology and an easy-to-use interface allow users of all skill levels to perform fast, accurate inspections—boosting performance and streamlining workflows. Proven to Perform, Trusted to Deliver An all-in-one imaging platform, coupled with unmatched portability and versatility, delivers exceptional results in even the most challenging inspection environments. Designed to Evolve with Your Needs With free quarterly software updates, the OmniScan X4 empowers you to continuously adapt to future inspection needs—ensuring that you’re always ready for what’s next. Scan to learn more
ims.evidentscientific.com