ISSUE 18: 2026
BEHIND THE SEAMS OF THE GLOBAL DENIM INDUSTRY
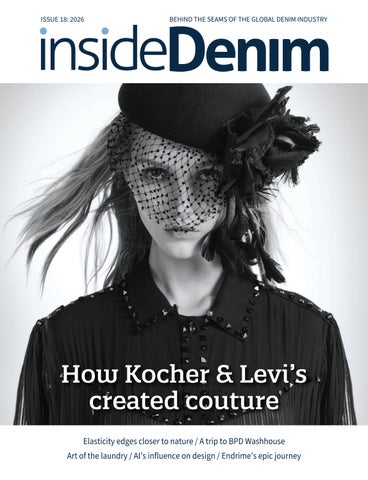
How Kocher & Levi’s created couture Elasticity edges closer to nature / A trip to BPD Washhouse Art of the laundry / AI’s influence on design / Endrime’s epic journey
INSIDE DENIM CONTENTS
Contents ISSUE 18: 2026
BEHIND THE SEAMS OF THE GLOBAL DENIM INDUSTRY
03
Editor’s letter: 06
Co-editor Sophie Bramel zeroes in on the close-knit community that keeps denim moving forward.
04 Global news Some of the top stories from around the world.
06 Guest comment: Claudia Giacovelli How Kocher & Levi’s created couture Elasticity edges closer to nature / A trip to BPD Washhouse Art of the laundry / AI’s influence on design / Endrime’s epic journey
Cover Christelle Kocher for Levi’s: Inspired by an archival workwear jumpsuit, this silhouette is reimagined in lightweight 4oz denim, with flat silk organza plissé inserts, digitally laser-cut indigo denim fragments and Swarovski crystals, involving 300 hours of handwork. A veiled bibi hat, by Maison Michel Millinery in Paris, ornamented with denim flowers and goose feathers, completes the look.
Drawing from her work with the Tunisian denim sector, Claudia Giacovelli from the United Nations Environment Programme says manufacturers need support to adopt cleaner practices at scale.
THE SCIENCE BEHIND THE STYLE
08
PHOTO: LEVI’S
Editors Sophie Bramel Clare Grainger Consultant editor Stephen Tierney
08
Suppliers are reducing synthetic fibres’ footprints by sourcing some of the ingredients from nature.
Publisher Simon Yarwood Design Tim Button Company secretary John Collins Editorial enquiries clare@worldtrades.co.uk sophie@worldtrades.co.uk
Alternative stretch
12
Dialogue: Nikita Raman Hugo Boss designer Nikita Raman says a deep knowledge of fabrics and processes, as well as your brand and customer, are essential to make product stand out.
16
Levis’ couture moment French designer Christelle Kocher applies the Parisian atelier treatment to denim.
16
18
BluConnection
27
Insidedenim.com
02
Lycra
BC
Sharabati
23
INSIDE DENIM CONTENTS
Advertisers Index
DENIM IN-DEPTH
Water management Australia’s cotton industry wants the government to stick with its current strategy, but to find ways to get better results.
Head Office World Trades Publishing, The Old Stone House, Teeton, Northampton NN6 8LH, UK. Tel: +44 151 928 9288
SCIENCE BEHIND THE FADE Around the world
24
The Endrime team rock up some serious airmiles as consultants and publishers… meeting a few denim friends along the way.
24
@insidedenimWTP
Jean Genie: The art of the wash
@insidedenimWTP
Leanne Jae tells us why understanding the laundry processes is the key to efficiency, precision and great outcomes.
28
@InsideDenim @insidedenimWTP
Connections and creativity World Trades Publishing 2026 Contributions: The editor welcomes news items, articles and photographs for consideration and possible publication but no responsibility can be accepted for the loss or non-publication of such material. Opinions expressed by individual contributors do not necessarily reflect the view of the editor or publisher.
Bill Curtin’s BPD Washhouse offers a space for experimentation and learning.
FACTORY TALK
30
30
Guts and glory Tilmann Wröbel travels to Spain, where he is seriously impressed by the Japanese-looking fabrics at Textil Santanderina.
32
Clocking On: Anu Wijesooriya CleanKore’s technical director, Anu Wijesooriya, take us through his working day, turning ideas into solutions with his brand and laundry partners.
Whilst every effort is made to ensure accuracy in reproduction, no responsibility can be accepted for the technical content or for claims made by manufacturers for product performance that are published. Publication in Inside Denim cannot be construed as an endorsement for a claim or product by the publisher. Graphic origination by WTP. Printed by Bishops Printers, Walton Road, Portsmouth, Hampshire PO6 1TR All rights reserved. ISSN 2633-9463 World Trades Publishing 2026. All rights reserved. No part of this publication may be reproduced, stored in a retrieval system or transmitted in any form or by any means mechanical, electronic, recording, photocopying or otherwise, without the written permission of the publisher. Inside Denim is published three times a year by World Trades Publishing, The Old Stone House, Teeton, Northampton NN6 8LH, UK.
01 ISSUE 18 / 2026
20
Sales Simon Yarwood Direct: +44 151 319 4977 Mobile: +44 7887 523872 Email: simon@worldtrades.co.uk
INNOVATIVE DYNAMIC ICONIC Inside Denim - where innovation, sustainability and business come together.
Advertise in Inside Denim to reach our global community – simon@worldtrades.co.uk
EDITOR’S LETTER
Stronger together Exploring new solutions with an open mind, aka creativity, is what sets Leanne apart. This issue’s Jean Genie is back with a detailed overview of the art of finishing. It hinges, she says, on sharing knowledge between designer, fabric technologist and laundry, and then letting go to see where a fabric and a process can lead. Creativity does not exist in isolation, she points out, echoing the mindset of Bill Curtin at BDP Washhouse. He is a driving force in bringing people together across the supply chain – including chemicals companies – as well as training the next generation of denim experts. Creatives have their eye on the future, as well as on any potential cracks in the system that could help to push boundaries and breathe new life into jeans. Christelle Kocher’s extravagant reworking of Levi’s jeans is a stunning example of where denim can go. The designer shares the universal love of jeans in the pieces she crafted for her couture collection. “I love the idea of bringing a touch of couture into everyday life. Denim makes that possible because it’s probably the most democratic fabric in fashion: something that belongs to everyone.” When he spotted big and bold denim fabrics at Santanderina, Tilmann Wröbel learned that they were inspired by the mill’s work with French designer Isabel Marant. This is yet another example of the positive impact of collaboration, and this he says is the oxygen needed to bring freshness to the denim industry.
Sophie Bramel Co-Editor / Technical Editor sophie@worldtrades.co.uk
03 ISSUE 18 / 2026
S
ince Inside Denim’s launch in 2020, supply chain disruptions have been a constant concern. A pandemic, roller-coaster freight costs and tariffs, more stringent transparency and sourcing regulations, particularly for cotton, and wartime upheaval of oil routes have each added a layer of complexity to a fiercely competitive market. Softer consumer demand has put further strain on a struggling industry. The closure of Orta’s mill in Turkey is a tragedy, as is Cone’s difficult decision to shutter its factory in China. There are bright spots, as we chronicle in these pages. Collaboration is the common thread cited by the industry luminaries we have reached out to. In a sector involving many different métiers, making connections and sharing knowledge is what makes denim magic for many. Endrime’s road trip is a perfect example of how closely knit the global industry can be. At the other end of the spectrum, an institution such as UNEP is also bridging divides in North Africa in support of better practices. Claudia Giacovelli, the organisation’s textile lead and this issue’s Guest Comment contributor, has much to say about the role each piece of the puzzle plays and the power of working together to deliver real impact. She notes that better data is needed to make better decisions. Artificial intelligence may offer a better tool for sharing information at all levels, as Nikita Raman of Hugo Boss tells us, a point of view shared by Leanne Jae at Blackhorse Lane Atelier.
DENIM GLOBAL NEWS
Global News France Rag & Bone, the denim brand founded by designers Marcus Wainwright and Nathan Bogle in 2002, has chosen the trendy upper Marais quarter of Paris for its third store in Europe, after openings in Amsterdam and Dusseldorf. Rag & Bone was acquired by Guess and WHP Global in 2024. Denim Deal has joined forces with United Repair Centre, a social impact company providing apparel repair services, giving members discounts for the Europe-wide services. The partnership launched at Denim Deal Days Paris, where brands met mills, repair specialists, innovators and circular-fashion experts to explore how post-consumer recycled cotton performs.
UK Fast fashion brand Nasty Gal, launched by Sophia Amoruso in 2006, and most recently a part of UK-based Boohoo Group, is being acquired by WSG Brands, a brand management company based in New York. WSG plans to expand Nasty Gal’s product offering by leveraging licensing in denim, footwear, bags and activewear.
Spain Hydroponic-farming company Magtech, backed by H&M Group’s Circular Innovation Lab, is testing growing cotton without soil and in a closed loop of water. HKRITA and Materra have explored versions of soilless or controlled environment cotton in the past. Magtech says its use of AI to monitor plants brings the cost down meaning scaling is a possibility. The first garments from this cotton have been made in Spain and a second site is under way in India.
Germany Specialty chemicals company CHT says sustainable products now account for 84% of its total sales, underlining the growing adoption of lower-impact textile processing technologies across the industry. The milestone, announced in the company's latest Sustainability Report, reflects increasing demand for solutions that help mills and laundries reduce water, energy and chemical consumption.
Turkey Turkish denim brand Mavi has reported flat revenues of £396 million for the first half of the year, but an improvement in profit. During the six-month period, the company expanded seven stores and upgraded 14 others, while also opening four stores in the US. It now operates almost 500 stores in 30 countries.
04 INSIDE DENIM
Italy Diesel and OTB founder Renzo Rosso, his family and friends attended the Venice Film Festival for the premiere of Be Brave, a 90-minute documentary about his life and the growth of the fashion companies. However, none of the footage of Rosso was recorded, it was generated through artificial intelligence. The story is woven together with interviews with friends and colleagues. Fendi has chosen to enhance its jeans with a measure of abacá fibre. The Italian fashion house’s A/W 26-27 denim collection is made from a blend of organic cotton and Bananatex, a fibre originally developed for and by Swiss brand Qwstion. The fabric is dyed and woven by Berto.
Orta will close its doors after 73 years – the current economic conditions meaning its operational model is not sustainable. Innovation has been a driving force at the mill – Inside Denim has reported on many pioneering developments, including a collection dyed with wool-waste dyes; a CO2-absorbing fabric; early commercial volumes of Lycra’s partially biobased elastane and Pili’s biobased indigo; indigo foam finishing and blockchain-based cotton. Orta said it will fulfil existing commercial obligations responsibly in alignment with its corporate values.
The global production of virgin fossil-based polyester across all end uses increased from 68 million tonnes in 2024 to 73 million tonnes in 2025, a 7% increase, according to the Textile Exchange. However, the 384 fashion brands that report into its Materials Benchmark collectively decreased their use of new virgin fossil-based polyester from 0.54 million tonnes to 0.48 million tonnes.
Brazil Natural Cotton Color produces varieties of cotton plants in various shades of brown and beige. These have been spun and knitted into fabrics with Lycra Renewable, a partially biobased elastane, by Texpar. The cotton is produced by a cooperative, ITACOOP, that works with 90 smallholder farms in Paraíba.
Pakistan The Organic Cotton Accelerator has united seed companies, research institutions, government representatives and textile stakeholders to develop a roadmap for commercialising non-GM cotton seed in Pakistan, with backing from Soorty. OCA’s Organic Seed Commercialisation project covers 100 acres, with expected production of around 40 tonnes of non-GM cotton seed. Artistic Milliners is investing in a unit at a new 400-acre apparel zone at Port Qasim, near Karachi. Ministers said the cluster would focus on high-value apparel, with the first phase alone expected to generate over 138,000 jobs and annual exports worth $2.2 billion.
Canada Canopy’s Hot Button Progress Report, which focuses on manmade cellulosic fibre practices, shows The Green Shirt [top] ranking now counts 22 of 28 producers screened, or 79%, up from last year’s 70%. The adoption of next-generation solutions - trading wood pulp for alternative feedstocks such as textile waste, agricultural residues and certified bamboo - is also up.
DENIM GLOBAL NEWS
US Wrangler has launched the Blue Bell collection, its first standalone entry into the premium space, made with Japanese selvedge. It draws its name from an early 20th-century workwear company that acquired the Wrangler brand in 1943.
Japan Denim group Japan Blue has told Inside Denim that despite doubling sales since 2022, it intends to carry on growing responsibly, to preserve the craftsmanship and quality that make Japanese denim unique. It is investing in a monozukuri hub – a space to promote both product and culture – which will strengthen its atelier functions. Aparks Zucchero Blue has developed a zero-waste manufacturing system based on a special flat seaming technique called Twin Prover Seam (TPS) sewing. As the selvedges are sewn edge-to-edge, there is no need for a seam allowance, which minimises fabric waste.
China Cone Denim will close its denim manufacturing operations in China by the end of this year, a decision motivated by “changing global trade dynamics, evolving customer sourcing strategies, cost pressures, supply chain considerations and broader geopolitical developments,” the company said. It will focus on its two facilities in Mexico.
India AltMat is developing a natural cellulose fibre that is made from crop waste. The patented process to create the natural cellulose fibre was seven years in the making. The company has been steadily scaling up from lab production in 2019 to pilot scale, and now to a 500 to 1,000-tonne-per-year factory located in Ahmedabad.
mill in Cambodia – integrating spinning, dyeing and finishing – covering both denim and piece-dyed fabrics. Around 70% of its water consumption will come from recycled sources. It will also recover steam and recycle over half its caustic soda.
05 ISSUE 18 / 2026
Cambodia China-headquartered Panther Denim is set to open a
GUEST COMMENT
“The solutions already exist. Now denim needs to scale them”
06 INSIDE DENIM
T
he denim industry is often shown as needing a sustainability breakthrough. In reality, many of the solutions already exist. Manufacturers can reduce water use through advanced washing technologies, replace hazardous chemicals with safer alternatives, increase recycled fibre content, improve energy efficiency, adopt renewable energy and invest in more circular production models. Across the sector, companies are already demonstrating that substantial environmental improvements are possible. But denim's challenge is also the challenge facing the wider textile industry. From cotton and wool to synthetic and cellulosic fibres, what many companies lack is clarity about which solutions to invest in first and, equally importantly, the conditions needed to scale those investments. This is one of the key lessons emerging from the United Nations Environment Programme's InTex programme, which works with textile and garment manufacturers to apply life cycle thinking to business decision-making. Increasingly, the transition towards sustainable and circular textiles is less about inventing new technologies and more about identifying the interventions that deliver the greatest impact and creating the conditions that enable them to succeed. Tunisia provides a compelling example. As a major supplier to European markets, the country's textile and denim manufacturers are navigating rapidly evolving expectations around transparency, traceability, product durability and environmental performance. Through our work with the sector, we have seen a clear willingness to adopt and invest in water recycling systems, cleaner production processes, safer chemical management and greater supply chain transparency. What stands out is not a lack of ambition. It is the difficulty of turning ambition into action. For manufacturers operating in highly competitive global markets, every sustainability investment involves difficult choices. Should limited resources be directed towards reducing water consumption, improving energy efficiency, increasing recycled content, upgrading machinery or strengthening chemical management?
GUEST COMMENT Claudia Giacovelli, country portfolio lead for textiles at the United Nations Environment Programme, says the challenge is creating the investment, commercial incentives and collaboration needed to take solutions from pilot projects to scale.
This is where life cycle thinking becomes essential. By assessing environmental impacts across the entire life cycle of a product, companies can identify where the greatest impacts occur and where investments are most likely to generate meaningful reductions in emissions, pollution and resource use. Environmental data is therefore not simply a reporting requirement. It is a strategic tool that helps businesses prioritise action, identify resource and energy savings, reduce compliance risks and position themselves for growing demand from brands and markets that increasingly value transparent and lower-impact products. Yet better data alone will not transform the sector. Once manufacturers understand what needs to improve, the greater challenge is making those improvements financially and operationally viable. As we’ve seen with our work in Tunisia, often factories have to choose between implementing, say, a laser machine for producing effects on denim or installing a photovoltaic system for solar power. This is because across textile-producing countries, producers operate under intense cost pressures, narrow margins and fierce international competition. At the same time, expectations from governments, brands and consumers continue to grow. Companies are being asked to improve environmental performance, strengthen traceability, comply with new reporting requirements and invest in circularity, often while remaining competitive on price in challenging market conditions. This creates a fundamental tension at the heart of the denim and broader textile transition: the costs of environmental improvements are frequently borne by manufacturers, while many of the benefits are unevenly distributed across the value chain. As long as this imbalance persists, progress is likely to remain slower than what environmental goals require. This is only heightened by the sustainability paradox of textiles. A more sustainable pair of jeans is unquestionably an improvement. But if ever greater volumes of garments continue to be produced, sold, and discarded within the same linear model of take, make, use and dispose, overall resource consumption, emissions, pollution and waste will continue to rise. This is why the transition cannot focus solely on making sustainability improvements within a system that ultimately just improves the efficiency of linear business models. It must also accelerate the shift towards circular approaches that create value through durability, repair, reuse, resale and resource recovery.
The conversation must move beyond technologies and pilot projects. The question is how to make their adoption economically viable at scale within a more circular system… And that is a challenge that no manufacturer, brand, policymaker, investor or consumer can solve alone. Achieving this shift requires action from every actor in the value chain. Policymakers can help create clearer and more consistent regulatory frameworks that reward transparency, environmental performance and circular business practices. Financial institutions can expand access to financing for resource efficiency and cleaner production. But one of the most important roles belongs to brands. Sustainability cannot become an ever-expanding list of requirements passed down the supply chain without corresponding support. If brands expect suppliers to invest in cleaner technologies, lower-impact production processes and greater transparency, they must also help create the business case for those investments. Doing so can help secure more resilient supply chains, support regulatory compliance and unlock innovation that increasingly differentiates products in the marketplace. Longer-term sourcing commitments, fair purchasing practices and meaningful recognition for sustainability leaders can provide manufacturers with the confidence needed to invest.
Consumers also have a role to play. Demand for more sustainable products sends an important market signal. Equally important is moving beyond fast-consumption habits by choosing durable products, extending their lifespan and embracing more circular consumption patterns. Enhancing consumer awareness, including through consumer-facing tools that can draw on information provided through digital product information systems like the EU Digital Product Passport (DPP), and engaging in more sustainable marketing practices can go a long way in this regard. The next chapter of denim's sustainability journey, and that of the textile sector more broadly, is not about invention. It is about implementing circular systems at scale.
GUEST COMMENT
The costs of environmental improvements are frequently borne by manufacturers.
07 ISSUE 18/ 2026
PHOTO: CLAUDIA GIACOVELLI
SCIENCE BEHIND THE STYLE
In just a few years, renewable, recycled and natural raw materials have given stretch yarns a greener profile. The technologies are operational, production is scaling up, and matching the cotton in denim with another plant-based yarn feels natural.
Stretch solutions bet on plant over fossil
08 INSIDE DENIM
I
t is more than just a trend when new factories come out of the ground. Korean fibre producer Hyosung has invested $1 billion in a facility that produces biobased butanediol (bio-BDO), a key component of elastane, or spandex. It is now up and running in Ho Chi Minh City, Vietnam, close to a Hyosung elastane plant, further reducing the environmental impact of its regen Bio Elastane. Its announced capacity is 50,000 tonnes annually, and the group says it is prepared to increase this to 200,000 tonnes if market demand follows. The Lycra Company is also delivering a bio-derived elastane, Renewable Lycra fibre. Its launch was made possible by the construction of a 66,000-tonne-per-year bio-BDO plant in Eddyville, Iowa. A $300 million investment by Qore, jointly owned by Cargill (US) and HELM (Germany). The corn used to feed the facility is sourced from farmers located within a 100-mile radius. This April, CovationBio, a company spun off of DuPont and now owned by Chinese textile group Huafon, inaugurated a new 50,000-tonne facility producing bio-PTMEG, another chemical used to make elastane. It is part of a RMB 10 billion (or €1.2 billion) multi-phase investment plan. Xatryx, which is described as a drop-in replacement for fossil-based PTMEG, is now commercially available. It is the fruit of “a new-to-the-world process called Advanced ThermoChemical technology that was developed in-house by CovationBio,” says Mosha H. Zhao, marketing director for the C4 Platform that produces the compound. CovationBio has experience in the biobased stretch yarn market through its Sorona brand, a PTT fibre that is 37% biobased and launched in the early 2000s. Shinkong Synthetic Fibers recently launched commercial production of Neolast at a brand-new production facility in China. The polyester-type stretch yarn was launched by US fibre producer Celanese with sports brand Under Armour in 2024. An elastoester fibre, like Sorona and Lycra T400, it can be recycled in polyester waste streams. Celanese is working on denim fabric developments with mills in Italy and Turkey.
Production of Hyosung’s regen Bio Elastane has begun in a new factory in Vietnam that is part of an integrated supply chain, contributing to lower carbon emissions and speed to market. PHOTO: HYOSUNG TNC
Both the Qore and Hyosung bio-BDO plants use a technology developed by US biotech company Genomatica. For non-chemists, BDO and PTMEG are both needed to make elastane, a type of polyurethane. Along with MDI (too complicated to spell out here), they form the polymer’s combination of soft and hard segments, which gives it its stretch and recovery properties. With CovationBio producing a bio-PTMEG, Huafon, a major producer of stretch yarn, can now also develop a bio-elastane. Switching to bio-derived PTMEG can lead to a reduced carbon footprint of up to 44%, according to a 2022 screening life cycle assessment by The Lycra Company. Hyosung is currently conducting LCAs for both BDO and spandex, with results expected in early 2027. “Based on preliminary internal estimates, regen Bio Elastane is expected to deliver a reduction in carbon emissions of approximately 45%–55% compared with virgin spandex,” says Jay Woo Lee, denim lead at Hyosung TNC, adding that these figures remain subject to change until the assessments have been completed.
SCIENCE BEHIND THE STYLE PHOTO: THE LYCRA COMPANY
09 ISSUE 18 / 2026
The Lycra Company’s Lycra VintageFX offers controlled comfort stretch (rather than simply more stretch) and authentic vintage aesthetics with improved movement and recovery. A biobased, Renewable Lycra version is also available.
SCIENCE BEHIND THE STYLE 10 INSIDE DENIM
CovationBio’s Sorona is technically an elastoester fibre (or elasterell-p in the US). The bicomponent yarn is said to deliver permanent comfort stretch and long-lasting shape retention. PHOTO: COVATIONBIO
XLANCE, in Italy, now offers a biobased version of its polyolefin stretch fibre. “Our new version of XLANCE uses bio-circular feedstock derived from waste streams, including used cooking oil, rather than virgin fossil feedstock. It is 100% bio-circular, and the supply chain is verified through ISCC PLUS certification,” says XLANCE brand manager Filippo Colnaghi. “We prefer the term ‘bio-circular’ to ‘biobased’ because the feedstock comes from biological waste and residues. This means we can reduce dependence on virgin fossil resources without using agricultural land or competing with food production.” The feedstock used to produce biopolymers often raises the sensitive issue of land use and food sovereignty. Despite the allure of a lower carbon footprint, some brands and corporations are reluctant to switch to fibres made from plants from agro-industrial sources. CovationBio now uses corn cobs, a non-food feedstock, to produce its Xatryx bioPTMEG. Hyosung has replaced corn with sugarcane, which it sources from Brazil, where there is overcapacity in sugar production, says Simon Whitmarsh-Knight, Hyosung Textile’s marketing and sustainability manager. This change also removes a step from the production process, as corn needs to be converted into sugar. The group offers two bio-elastanes: one with 70% biobased content, the other 98% biomass-derived, thanks to a combination of 70% from sugarcane and 28% from mass balance plant-based biomass.
Rubber revival As Yulex prepares to launch its Yulastic yarn in denim, Candiani’s Coreva is no longer the only natural rubber-based stretch yarn in the sector. The Seattle-based company’s natural rubber filament is made from a patented latex purification process. Yulex sources its rubber from smallholders and cooperatives in Southeast Asia. Tests comparing elastane and rubber found the natural stretch yarn had a higher recovery rate of 94% versus 80% (using ASTM D3107, Stretch Properties of Fabrics Woven from Stretch Yarns, and ASTM D4964, Tension and Elongation of Elastic Fabrics). The fibre can be used in proportions comparable to that of elastane. Pakistan-based Artistic Milliners has been testing the yarn. “Yulastic shows better recovery after stretch compared to petrochemical-based elastane. It bounces back into shape more consistently over repeated wear and wash cycles. This is important for denim, where recovery performance over the life of the garment is often a pain point,” says Baber Sultan, Artistic Milliners’ product manager and head of R&D. He adds that fabrics made from the fibre retain denim’s innate character and aesthetics. At laundry and finishing stages, Yulastic denims also withstand processing conditions well. “We have found good resistance to both heat and bleach. This gives mills flexibility in finishing without worrying about degrading stretch performance,” he says.
Yulex is working with Artistic Milliners to bring its natural rubber Yulastic filament to market. PHOTO: YULEX
The switch to renewable resources is also an opportunity for greater transparency, notes Jay Woo Lee, at Hyosung. “Our goal is to create denim that combines more sustainable and traceable materials with genuine consumer comfort. Our regen BIO Elastane offers greater transparency regarding the origin and environmental value of its raw materials while maintaining the stretch, quality and comfort of conventional products.” Kiki Chen, in charge of marketing communications for Sorona Apparel at CovationBio, also sees “exciting opportunities in combining Sorona with natural fibres to enhance their performance while maintaining their natural comfort and aesthetics. Sorona brings together the best of nature and performance.” Although they are more expensive, due to the additional cost of converting biomass into high-performance chemicals, the new bio-elastane yarns are described as drop-in replacements for standard spandex. “This helps minimise the additional development work and manufacturing adjustments often associated with introducing a new material,” points out Mr Woo Lee. Stretch yarns are a small component of a pair of jeans but they are essential and ubiquitous. While eco-design guidelines may recommend keeping elastane content under 5% to allow for recycling, elasticity equates with comfort. It is a given, and for many mandatory. The sums invested in high-tech factories to produce biobased stretch yarns confirm the importance of a market estimated to be worth between $7 billion and $9 billion. Brands looking for materials with a lighter carbon footprint now have access to fully commercial biobased elastane. It is more prevalent than recycled spandex, which is in short supply. Alternative, non-spandex and non-petrochemical stretch yarns are also moving into denim with their own set of performance and sustainability claims. Elasticity plays an outsized role in jeans. It can now add another benefit to the value it creates: making blue jeans greener.
SCIENCE BEHIND THE STYLE
Next gen stretch fibres Behind the scenes of the industrial scaling of bio-elastane, several start-ups are developing non-petrochemical stretch yarns. Tera Mira, based in London, is tapping algae. “Unlike corn and sugarcane, seaweed is a climate-resilient organism that doesn’t require fresh water or land,” Jeanne Begon-Lours, co-founder, tells Inside Denim. First iterations of the fully biobased yarn present the requisite stretch and recovery properties. “We have the stretch and the recovery, but the yarn lacks strength, and this doesn’t make it a good match for denim’s laundry processes,” she concedes. With Lucy Dain-Williams, CTO and co-founder, the pair sees potential not in imitating elastane, but in investing in the algae-derived stretch fibre’s inherent and unique properties. Alginate fibres are naturally flame retardant, good at moisture wicking and biodegradable. This could make Tera Mira’s stretch yarn useful in workwear and next-to-skin applications. Nanoloom, a start-up also based in London, has eyed graphene to make a non-fossil fuel, non-toxic and biodegradable stretch yarn. Its fibres have demonstrated 100% post-stretch recovery and high tensile strength. Company founders Victoria Mataczynski and Alexander Seifalian have been working with activewear brand Gymshark to bring the innovative fibre to market.
XLANCE, which is available in petrochemical or bio-circular versions, is in trials at US and European brands. PHOTO: XLANCE
11 ISSUE 18 / 2026
A better match? Stretch performance over time is often an issue in jeans, and some non-elastane stretch yarns offer greater resistance to the wear and tear that denim products typically undergo. “The bio-circular XLANCE has been developed to deliver the same technical performance as conventional XLANCE. That means the same long-lasting stretch and recovery, with XLANCE's characteristic resistance to heat, UV exposure, and aggressive chemicals and treatments,” says Mr Colnaghi. Neil Bell, who works for the company, notes that “we’re solving the problems of bagging and loss of stability after home laundry, which brands appreciate”. Although elastane makes up a small portion of a pair of jeans, a plant-derived version may be a better match for cotton. “For brands and mills, the real draw of Renewable Lycra fibre is that they can increase the plant-based content of the stretch component while continuing to use familiar fabric constructions, manufacturing processes and garment patterns,” says Ebru Ozaydin, head of denim and ready-to-wear at The Lycra Company.
DIALOGUE
Nikita Raman, a senior designer at Hugo Boss, considers how AI, sustainability, and commercial strategies are changing the design process. While embracing new technologies, she believes the future of great denim remains rooted in fabric, craft and experimentation.
12 INSIDE DENIM
Designers’ next dimension How much impact is AI having on the role of a designer? Where do you think it has benefits and limitations? Generally, AI, like most technologies, is created to make our lives easier. One of the AI memes I’ve seen was from author and video game enthusiast Joanna Maciejewska: “I want AI to do my laundry and dishes so that I can do my art and writing, not for AI to do my art and writing so that I can do my laundry and dishes.” I think the same applies to designers. The best part of being a designer is developing concepts and finding new ways to bring them to life. Unfortunately, alongside that comes a lot of administration: tech packs, follow-ups and, in some cases, endless system work. This is where I see some of AI’s biggest potential. Rather than asking what AI can design for us, designers could look at their own process and ask where AI can support it. Draped styles can be simulated to better communicate an aesthetic to a pattern-maker. Silhouettes and key looks can be built quickly, and garments can be tested across different body types to give an indication of proportion and fit. There is also potential beyond the creative process. I recently read an interesting example about communication with suppliers across different time zones. If relevant design and technical information were available within an AI-supported system, suppliers could potentially get answers to certain questions without waiting for the design team to come back online, particularly useful when production is waiting for a decision. AI still has its limitations. At the moment, working with it can sometimes feel frustrating, like working with a teenager: selective hearing combined with a tendency to take instructions far too literally, although I suspect this will improve as the technology develops and we become better at communicating with it. Personally, I’m all for digital development, but I don’t believe a creative garment should begin digitally. Working directly with fabric on a body sets a higher standard for what can later be digitalised. Pattern-making is a good example: paper patterns, mock-ups and fabric draping remain an art form. Technology can support that craft, but the physical understanding of how fabric behaves is still what creates a better garment. Over the next few years, I think the conversation will increasingly move towards the ethical implications of AI and questions around creative ownership. There is also a sustainability question around AI that I think we need to take more seriously. We are becoming increasingly aware of the electricity, water and physical infrastructure required to support AI, but there is still relatively little transparency around the environmental impact of our everyday use. AI can feel a little like the Wild West: adoption is moving faster than our understanding of its consequences. In fashion, we have spent years questioning the impact of materials, processes and supply chains. I think we should bring that same critical thinking to digital tools. If AI helps us reduce unnecessary sampling, improve decision-making or work more efficiently, there can be a clear benefit. But generating endless images simply because we can is a different conversation. For me, the next step is education and transparency, so designers can make conscious choices rather than assuming that digital automatically means sustainable.
AI can feel a little like the Wild West: adoption is moving faster than our understanding of its consequences.
Nikita Raman: “We have spent years questioning the impact of materials, processes and supply chains. I think we should bring that same critical thinking to digital tools.” ALL PHOTOS: NIKITA RAMAN
Advances in AI can help designers with the more laborious tasks but Nikita urges caution when applying it to creativity.
DIALOGUE
How can we improve the flow of knowledge between brands, mills, garment-makers and chemical suppliers? I think the best way is simply to share more of it. Everyone involved in making a product has their own expertise, and as a designer I don’t need to know everything, but I do need to know who to bring into the conversation. I’m a big believer in getting people out of their individual corners. Bring your garment-makers to fairs. Introduce them to mills and chemical suppliers. Organise workshops and experiment together. Explain what you are trying to achieve but also be curious about what they know that you don’t. I’ve seen this work well in practice. At a fair, I saw wash effects from a chemical supplier that were exactly what I was looking for. I introduced them to our garment maker, and we organised a workshop together. We brought the raw garments, I explained the aesthetic I wanted, and the chemical supplier developed the washes while sharing their technical knowledge with the garment maker’s wash expert. The collaboration continued afterwards, with the chemical supplier visiting the garment-maker to help translate those trials their own laundry. That step is important because you can’t simply copy a wash from one place to another. Equipment can be different, but so can the water, climate and working conditions. You must adapt and find out what works in that environment. That’s what good collaboration looks like. You’re not asking everyone to execute their own isolated part; you’re bringing different expertise together, sharing knowledge and learning from each other. And sometimes that leads you to a product or solution you wouldn’t have discovered on your own.
13 ISSUE 18 / 2026
What changes have you seen in your career driven by improved technologies or processes? How much do the financial or marketing strategies of a brand feed into new designs and inform creative direction? Most companies work with a collection structure that ranges from core basics to more directional fashion pieces, all shaped by the overall brand strategy. What I’ve seen change over the years is the increasing involvement of the designer beyond the purely creative part of the process. This varies from brand to brand. I’ve worked at companies where I could follow a product from initial concept through development and beyond, while others involve the designer at more specific stages. Coming from the denim industry, technical sketches and tech packs have always been a natural part of my design process, although some designers and brands still rely more heavily on hand sketching. I still work with technical sketches today, but the toolbox around them has expanded considerably. Digital development has given us new ways to communicate and develop ideas, and now we’re starting to explore where tools such as AI can support that process too. For me, it’s less about replacing one way of working with another and more about having more tools available and knowing which one is right for the job. Perhaps the bigger evolution, though, is what is expected from a designer. There is an increasing need for technical and business knowledge alongside creativity. Financial targets, commercial performance and marketing strategies inevitably influence a collection, but I don’t necessarily see that as a restriction. Understanding costs, production realities, the customer and the wider brand strategy allows you to make more informed creative decisions. Fabric is a good example. When margin becomes a challenge, fabric can be one of the first areas where you look for savings. But particularly in denim, fabric, fit and wash are deeply connected. Changing the fabric can completely change how a garment fits, feels and washes. Saving in one area can therefore have consequences for the overall product, which is where the designer needs to understand both the creative and commercial sides of the decision. Ultimately, creativity doesn’t exist in isolation. A great idea still needs to become a great product, make sense for the brand and connect with the customer. For me, that isn’t about becoming less creative or simply more commercial, it’s about designing more intelligently.
DIALOGUE
I do think there is a risk of product becoming more homogenous when so much of the market is responding to the same trends at the same time. For me, differentiation comes back to understanding who you are as a brand, but just as importantly, understanding your consumer and what they need from you. That’s also where I think designers can bring a lot of out-of-the box thinking. We can all see the same trends, but how you interpret them through your own brand codes, identity and consumer can lead to completely different results.
Down time: The knowledge behind weaving techniques helps designers understand their fabrics more implicitly.
14 INSIDE DENIM
Mills will often present single fabrics that can be washed to create various iterations and used for different designs. How does your creative mind approach this, and will this become more common as more brands move to cost cutting? This connects quite closely to the previous question. For me, working with one versatile fabric is simply a different kind of creativity. Limitations, or even being given a fabric I wouldn’t naturally choose myself, can actually make the process more exciting because they push me to explore denim differently. Understanding what a fabric can and cannot do is a big part of that. One fabric can already give you very different results through wash, cast, tinting and finishing. I also like looking at fabrics as families. You might work with similar yarns and compositions but explore different weights or weaves. There is a common base, but still a lot of room to play and create very different expressions. I do think we’ll see more brands working this way as they look to simplify their fabric offers and control costs. The interesting part is finding a versatile fabric or fabric family that works creatively as well as commercially, rather than simply reducing the number of fabrics. How can designers differentiate product? Is everything becoming too homogenous? I used to look at denim back pockets to differentiate between brands. Working for Lee Jeans trained my eye to immediately spot a Lazy S, along with the signature details of other iconic denim brands. Those small codes can create a surprisingly strong identity. Consistent brand details are still a great way to differentiate product, but in denim it can go much deeper than that. Fabric construction, weave and even the cast of the indigo can become part of a brand’s identity although recognising a brand by its cast or weave might be a particular talent reserved for denim designers!
How does ‘performance’ denim feed into this? Performance innovation often starts with a need, whether that’s greater comfort, durability, protection or simply making a garment work better for the person wearing it. So, for me, performance denim brings us straight back to the end consumer. Our lifestyles are becoming more dynamic, so why shouldn’t our jeans keep up? Looking at how people live in their denim can open new opportunities. Combine those needs with the creativity of a designer, and inspiration from both inside and outside the denim industry, and there is a lot of potential. Sometimes it can start with something as simple as asking: what do you wish your jeans could do? A personal example: I love dark colours, even in summer, but my favourite heavy, dark jeans are simply too hot to wear when temperatures rise unless I plan on spending the entire summer in air conditioning. I’m still searching for the perfect UV-protective, heat-managing dark denim that I can comfortably wear all year. I’ll happily volunteer as a test subject! The interesting part is then looking at where the solution might come from. Other industries have already spent years exploring fibres and technologies around temperature, protection, movement and comfort. Bringing some of that knowledge into denim and seeing how we can interpret it for a completely different product, opens up possibilities we haven’t fully tapped into yet. Who would you class as the visionaries shaping the industry? For me, visionaries are the people who see possibilities beyond what we already know. They question how things are done, try new approaches and, importantly, bring others along by sharing what they learn. David Tring is one person I would mention when talking about this topic. I admire his ability to connect the dots, combining years of industry knowledge with ideas and inspiration from outside the fashion world, while connecting with the next generation and embracing new tools and digital exploration. There is a curiosity in the way he looks beyond the denim industry and recognises what could be relevant within it. That same curiosity is something I had the opportunity to experience while working with the late Adriano Goldschmied and his team. What inspired me most was how, after decades in denim and such an incredible history within the industry, he still seemed driven to challenge what we knew, look for new possibilities and ask what denim could become next. There is also an incredible amount of knowledge and creativity sitting behind the scenes in this industry, among designers, technicians, wash experts, mill developers and makers who are experimenting, solving problems and developing ideas every day. They might not always be the people we hear from most, but their knowledge and contribution shouldn’t be underestimated.
DIALOGUE Brands seem wary of using language reflecting more “sustainable” fibres or processes for fear of greenwashing. What impact could this have in terms of take-up? How are designers having to change their thinking in view of upcoming regulations? For designers, I think the starting point is understanding which regulations are coming and what they mean for the product. That sounds obvious, but regulatory language isn’t always written for the common ear. What I’ve found helpful is when companies take that information, simplify it and translate it into what it means for people’s day-to-day work. Regular, short updates can be much more useful than expecting every designer to work their way through pages of legislation. It’s difficult to adapt your thinking if you don’t really understand what you’re designing towards. I’m personally quite sceptical about relying too heavily on sustainability communication at garment level. I think most people initially buy a garment because they like it, it fits well and they feel it offers good value. A sustainability message alone is unlikely to change their mind about a product they otherwise wouldn’t buy. At the same time, sustainability communication has become increasingly difficult for consumers to navigate. You might buy something believing it represents your values, only to read later that the brand has been accused of greenwashing. With so many different claims, certifications and messages, it can be difficult to know what to trust. Perhaps that caution around sustainability language isn’t entirely a bad thing. Personally, I’m more convinced by brands that communicate results rather than promises. Instead of putting the sustainability story onto every individual garment, I find it more meaningful when a brand can show measurable progress over time, what they have changed, what they have achieved and, equally, where there is still work to do. I remember interviewing with a brand that took this approach, and it really resonated with me. Their communication focused less on promoting the sustainability credentials of individual products and more on showing the progress of the business. It feels more transparent and gives a clearer picture of what the brand actually stands for. For me, though, the product still must come first. People need to genuinely want to buy it, wear it and keep it. Responsible choices and communication can add value to a good product, but they can’t compensate for a product people simply don’t want.
You have said you are interested in “letting the elements shape denim”. Can you expand on this, what processes fall into this category and where do you see the demand? Part of what makes denim so interesting is how it changes over time. Sunlight, water, wear and simply living in it all leave something behind. I think there is still a lot to discover by deliberately bringing those elements into the design process and seeing what they can do. There are already some fascinating examples of people experimenting with this. Rowan from Denim Research has exposed jeans to the British weather for six months, creating beautiful natural bleaching effects reminiscent of washes you see from Japanese mills. Korean designer Jiyong Kim explores a similar idea through sunlight, naturally bleaching and transforming garments in different colours. And it doesn’t stop with sunlight. Visvim has experimented with mud dyeing, combining it with indigo and craftsmanship to create something that feels very premium. Then there are much more spontaneous experiments, like Barbara from Life in Jeans jumping into the ocean wearing her jeans just to see what salt water, movement and drying would do to the denim. I love that idea of not knowing exactly what the outcome will be and simply seeing what happens. For me, that’s really what letting the elements shape denim is about. Giving sun, rain, salt, mud and time a role in the process and allowing a certain amount of unpredictability into the result. You create the conditions for something to happen, but you don’t necessarily control every mark it leaves behind. I think there is an opportunity for this, particularly when people are looking for something more individual. The fact that the results can be difficult to reproduce exactly can become part of their appeal. It brings together experimentation, craftsmanship and storytelling in a way that feels very natural to denim and there are probably still plenty of happy mistakes waiting to be discovered.
15 ISSUE 18 / 2026
As denim becomes more prevalent in high-end collections, how is the perception of luxury or premium denim changing? As we see more denim appearing in high-end collections, and more brands use the word ‘premium’ to differentiate their denim offer, I think it becomes increasingly important to understand what premium or luxury denim means. For me, premium should mean something beyond the standard offer, where the added value can be experienced in the product itself. It isn’t simply about a luxury price point. What differentiates truly premium denim is the level of design expertise and thought that goes into the complete product, from fabric and fit to construction, finishing and trims. It’s also about exploring new perspectives, whether through technology, craftsmanship, pattern cutting or finishing. Experimentation is an important part of that. You don’t always need to know exactly where you are going; trial and error can lead to happy mistakes and unexpected results that open up completely new ideas. The expertise lies in recognising their potential and knowing how to develop them further. That kind of elevation takes time. Premium denim isn’t created by simply adding more expensive materials or details; it comes from considering the product as a whole and using denim to express the premium identity of the brand.
DENIM IN-DEPTH
Designer Christelle Kocher worked with Levi’s to show how beautiful and versatile the “democratic” fabric can be when given the same attention, time and craftsmanship as the most precious materials at a Parisian atelier, with a 10-piece capsule making its debut at Haute Couture Week.
Denim’s couture makeover
W
16 INSIDE DENIM
hen fashion powerhouses combine with disruptive vision and world-class craftsmanship, extraordinary things can happen. 'Christelle Kocher for Levi’s' is a spectacular collection driven by the creativity of the French designer, underpinned by Levi’s industrial knowledge, and enabled by around 3,500 hours of handwork at Maison Lemarié, a Chanel-owned métier d’art. “I've always been fascinated by denim because it's such a universal material,” Kocher tells us. “What interested me was not simply decorating it, but exploring its untapped couture potential.” A graduate of Central Saint Martins in London, Kocher has worked with some of fashion’s most influential houses, including Bottega Veneta, Dries Van Noten, Chloé and Giorgio Armani. As artistic director of Maison Lemarié for 17 years, she helps preserve exceptional craftsmanship spanning featherwork, flowers, embroidery and textile innovation. In parallel, she founded her own brand, Koché, in 2015, bringing couture values into a more inclusive and contemporary setting and working to make craftsmanship more accessible. Its shows often take place in unconventional venues, such as at a transport hub in Paris and in underground markets, rather than in traditional fashion venues. In 2019, she was awarded the prestigious ANDAM Grand Prize. “I've always believed that couture shouldn't be confined to exceptional occasions,” she says. “I love the idea of bringing a touch of couture into everyday life. Denim makes that possible because it's probably the most democratic fabric in fashion: something that belongs to everyone.” The challenge was to transform the material without losing its identity, letting the fabric evolve through texture, movement and construction. To ensure this, she tapped Levi’s own experts, working with its pattern-cutters and innovation experts at the Eureka Lab in San Franscisco, designing custom colours and combining laser work with the techniques of Lemarié. Every intervention respected the character of denim while revealing possibilities people don't usually associate with it. “For me, couture is a way of working,” she says. “It's about time, precision, craftsmanship and emotion. If you approach denim with that mindset, it naturally becomes a couture material.” Parisian savoir-faire The capsule transforms Levi icons from the 501 to the Type II Jacket into highly crafted pieces, as well as pushing more elevated silhouettes. A long white denim skirt is entirely hand-embroidered with Swarovski cup chain, pearls and crystals. A gown of silk plissé panels is embellished with thousands of tiny laser-cut denim fragments individually placed between the pleats. A cropped couture bolero is composed of hand-crafted denim flowers, each one individually cut, hand-painted and finished with crystal-embroidered stamens, while a base of ostrich feathers, goose feathers and frayed denim creates texture and depth. Accessories extend the narrative. The Viridian Green Baby Brooklyn Bag has been hand-crafted from denim flowers, featherwork and frayed silk chiffon; while denim and silk chiffon petals and leaves on a dramatic cape have been individually hand-frayed to evoke the lightness of feathers. “Levi's carries an incredible cultural history and authenticity,” says Kocher. “Bringing that together with the extraordinary craftsmanship of the French maisons d'art felt very natural to me. Rather than opposing luxury and everyday clothing, I wanted them to enrich each other.”
High-end execution Five-hundred hours of handwork went into the first taster of the collection: a sculptural strapless gown crafted from black stretch denim with an exclusive iridescent finish, worn by German model Toni Garrn at the Cannes Film Festival in May. Thousands of laser-cut denim scales were meticulously reassembled by hand, creating texture and depth. Two months later, the 'Christelle Kocher for Levi’s' capsule debuted at Haute Couture Week in Paris, a feat Mathilde Vaucheret, Levi’s vice-president for marketing in Europe, described as a “major moment” for the brand. The response was overwhelmingly positive. Vogue included the collaboration among the developments of the autumn 2026 couture season and listed “couture denim” as one of the season's trends, noting Jean Paul Gautier and Ronald van der Kemp are also working to change its perception. “I hope this collection reminds people that beauty can exist in familiar objects,” adds Kocher. “Sometimes, all it takes is a different gesture, a different way of looking at a material to discover something unexpected. If these pieces bring a little magic into everyday life, then I've achieved what I set out to do.”
DENIM IN-DEPTH PHOTOS: LEVI’S
17 ISSUE 18 / 2026
Designer Christelle Kocher: “Sometimes, all it takes is a different way of looking at a material to discover something unexpected.”
DENIM IN-DEPTH
Water worries
18 INSIDE DENIM
C
otton Australia, the main representative body for cotton growers there, has contributed a detailed submission to a review of national water conservation strategies. Australia approved a far-reaching programme through its Water Act 2007. Almost 20 years on, it is this act that is now subject to a formal, independent review. In its submission to the review, Cotton Australia has argued that the focus should be on “getting better results from the system we have”, rather than what it called “another round of major changes”. General manager of the organisation, Michael Murray, says the review offers an opportunity to take stock of what Australia has already achieved and focus on what will make the biggest difference now to farmers and to rural communities. “We need to focus on getting better outcomes from the system we have,” Mr Murray says, “while giving growers and regional communities the certainty they need to plan for the future.”
The representative body of cotton farmers in Australia has said an independent water review should focus on full implementation of current water management policies rather than try to develop new ones. Millennium Drought Australia brought in the Water Act 2007 because the start of this century was a time of a severe lack of rainfall, especially in the south and south-east of the country. This period is now known as the Millennium Drought. This began in the late 1990s following a strong El Niño weather pattern in the winter (July and August) of 1995. By 2003, reports were calling it the worst drought since Europeans first settled in Australia. It took until 2010 or 2011 for the drought to break. Cotton-producing regions were severely affected. Records show that cotton farmers in Menindee in New South Wales and Biloela in Queensland, for example, reported zero cotton production at times during this period.
PHOTO: COTTON AUSTRALIA
We need to focus on getting better outcomes from the system we have while giving growers and regional communities the certainty they need to plan for the future.
DENIM IN-DEPTH
Australia’s department of agriculture, water and environment has said cotton farmers in Australia have water-efficiency levels that are three times better than the global average.
MICHAEL MURRAY, COTTON AUSTRALIA
What the cotton industry has asked for Cotton Australia’s submission sets out 24 recommendations covering water entitlements, markets, environmental outcomes, planning, regulation and regional communities. The recommendations include an appeal to have market needs as the number-one priority when the authorities take decisions on reallocating water resources from one state to another. The list also includes a request that “genuine stakeholder consultation” take place before and after any new legislation on water is drafted. The cotton organisation also calls on the federal government of Australia to resist “tilting its focus” towards the environmental ambitions that the 2007 act lays out. Its fear is that this would come at the possible expense of social and economic outcomes, which Cotton Australia argues are just as important. Of course the environmental aims are important too. In some cases, Australia has obligations under international treaties to preserve wetlands, to protect migratory species and so on. “The Water Act remains fundamentally fit for purpose,” Cotton Australia insists. “The next phase should focus on practical implementation, evidence-based decision making, market confidence and long-term resilience. Continued investment in infrastructure, environmental delivery, community capacity and transparent governance will provide greater returns than further regulatory complexity.”
19 ISSUE 18 / 2026
There are widespread reports of the El Niño weather pattern that is developing now being the strongest on record and this has led to speculation, in Australia and elsewhere, of important consequences, including conditions being hotter and drier than average in the southern hemisphere summer of 2026-2027. The official line from Australia’s Bureau of Meteorology is that no two El Niño patterns are the same and that a strong El Niño does not necessarily mean drought in Australia. There have been occasions when a strong El Niño has led to more, not less rain there. “El Niño is only one factor,” the bureau insists. In any case, this is not the reason for holding a review of the Water Act 2007 now. There was a stipulation in the 2007 act for a review to take place within 20 years; this is why the government has set up scrutiny of it now. The independent review launched in March 2026. There was in-depth consultation with representatives of Australia’s first nations in May, followed by a public consultation exercise that finished in August. There will be a draft report in November, with a final report going to government ministers at the end of February 2027.
Better than average Setting the scene for the cotton sector’s contribution to the consultation, Michael Murray explains that the organisation he leads represents around 1,500 cotton growers. For context, the Indian government puts the number of cotton farms there at around 6 million. Australia’s cotton industry has been the subject of praise from the national government, specifically from the department of agriculture, water and environment, which has claimed producers of the fibre in Australia have achieved water-efficiency levels that are three times better than the global average. Official figures also show that the water-use productivity (a reference to output for the volume of water consumed) of cotton farmers in Australia has improved by more than 50% since 1997. Nevertheless, even in Australia, cotton production is a significant user of water resources. Cotton Australia estimates that its members will consume between 6 million and 7 million litres of water per hectare. Most of Australia’s cotton farms are in the Murray Darling Basin. This is an area that covers more than 1 million square-kilometres of landmass, with six of Australia’s seven longest rivers flowing through it. In addition to cotton, it is of critical importance to food production in Australia. The effects of the Millennium Drought there led to the government to form a specific Murray-Darling Basin Plan after the Water Act 2007 came into law. Tensions built up because the federal government pushed to take over the management of the river system from the states (Queensland, New South Wales, Victoria and South Australia) and territory (Australian Capital Territory) that share the basin’s land and water. Some of those tensions remain.
SCIENCE BEHIND THE FADE
From vintage archives in New Mexico to the laundries of Kojima, Endrime’s Mohsin Sajid and Sadia Rafique brought together a remarkable international network of denim specialists to chronicle historic denim pieces and create a new visual and educational record of washing.
20 INSIDE DENIM
s 5 e 7 d a f n i d l r o w e h t Around H usband-and-wife team Mohsin Sajid and Sadia Rafique are the brains behind Endrime, a UK-based creative agency and brand that spans consultancy, education, marketing and design. Since the start of 2024, this work has included book publishing, beginning with documenting their own archive of historic denim articles and expanding into photographing and editing tomes for historical clothing experts; the books themselves have become collectors’ items. Having worked as a lecturer on university courses for 20 years, Mohsin could see a gap in the literature on denim washing and, together, the couple wanted to provide a resource for students, as well as established designers, to learn about how these looks are created, plus the history of how they had evolved.
Friend and former Orta wash manager Zennure Danisman was brought on board to design 75 washes that would demonstrate, for the first time, the chemistry and processes behind creative denim fades. Over several months, the team crisscrossed the globe to bring recipes to life, with the help of chemicals and wash experts, using fabrics from Artistic Milliners, Cone Denim, Orta, Indigo Textiles and Kaihara. “For the first time, many companies are giving away the secrets of how they create washes, all for denim education,” says Mohsin. The trips also included visits to the US to document important archives, as well as lecturing and consultancy visits. Here, Mohsin gives us a behind-the-scenes look at the work – people, processes and airmiles – behind the latest books from the Endrime stable.
ALL PHOTOS: MOHSIN SAJID / SADIA RAFIQUE
April 19: Sarcedo, Italy
Straight after Kingpins show in Amsterdam, we head to Tonello to start our biggest denim book project to date, ‘Born to Fade – Raw to Washed Denim’. We are working with Zennure Danisman, who has written detailed recipes, and Sadia and I have been photographing and filming each wash, it’s very exciting. We have been working with Tonello for the past four years on our SAKE Art Project, which Sadia leads. We have gotten to know Alice Tonello so well, it’s a lovely creative workspace, we feel at home going there and feel lucky to be working with denim master Massimo Falaguasta. The team there has created over 100 exhibition artworks for us, so washing just 15 garments is a breeze!
SCIENCE BEHIND THE FADE
T he road trip begins...
April 25: Kuala Lumpur, Malaysia Next stop, Malaysia, to help set up The CC, a new school and shared fashion space. I previously advised the organisers which sewing machines they should buy to work with denim and leather, sharing my wish list of 30. When I turn up in Malaysia, all the machines have been set up by co-founder Shaofen. I teach a group of students how jeans and denim jackets are made, a fun two days.
April 28: Tokyo, Japan From Malaysia, I head to Tokyo to launch the Japanese edition of one of our books, ‘Vintage Style Research’. Sadia spent weeks on the translation with David Cheng, one of the six collectors. To make this edition even more special, we created it as a hardback edition featuring a scan of 1890s jeans using Prosperity Textile’s WOW Cooltrans waterless print technology – the same technology they use to make the best printed jeans, in my opinion – and it turned out stunning. The best denim vintage shop, Berberjin, and possibly the best book shop in the world, Tsutaya T-Site in Daikanyama, ordered the edition. I got to meet lots of Japanese celebrities and denim fans at the launch event, a highlight of the trip.
May 9: Durango, US A quick trip home, now it’s over to the US. First stop is Durango, New Mexico, to start a project with one of biggest collectors of vintage mine-found denim, Brit "Indiana Jeans" Eaton. Brit’s outbuildings are packed with vintage denim, workwear, signs. It’s just mad. Our task is to photograph about 200 of the best vintage denim for a Denim Archive book. I can honestly say, I’ve never seen so much 1890s denim in one location! We did a five-day shoot, and hired collector and author Cory Piehowicz to help us.
May 12: Los Angeles, US
May 18: London, England After returning from LA, Sue and I start the Central Saint Martins denim project – the sixth year we have done this project together. Each student was tasked with making one virgin fabric garment and one upcycled piece from scraps and old samples, alongside portfolios and presentations. Once again, a superb set of students.
21 ISSUE 18 / 2026
Next, to Los Angeles, where we shoot for denim legend Maurizio Donadi. This involves over 200 garments all in shades of orange, and an entire collection of Champion sweatshirts for a second book. The orange book will be stunning as it’s helmed by another industry legend – Sue Barrett – who, alongside Sadia, will edit and refine the Maurizio Donadi archive book series. While in LA we also attended the launch of another book we put together, ‘Worker’ by Cory Piehowicz at RRL (Ralph Lauren) on Melrose Avenue. RRL stocks our Endrime books in its LA and New York locations. We were over the moon with this launch!
SCIENCE BEHIND THE FADE
June 15: Milan, Italy Zennure is back on the road with us. We meet her in Milan and head to Officina39’s facility in nearby Biella. Over five days, we work on 15 more washes for ‘Born to Fade’. If you have ever travelled to Italy, you know the hospitality these guys provide is the best. Owner Andrea Venier kept taking us out for extended lunch breaks and tours of his wonderful town. We have no idea how we finished another collection!
June 26: Boston, US Next stop, Boston, to work with denim specialist Dean Hashimoto. Together with Cory Piehowicz, we photograph his archive of 150 historical denim items over a weekend. Dean has written essays on each piece, so it should be fun to edit and put it together.
July 1: Tokyo, Japan From Boston, we fly directly to Japan for a 10-day trip. Our friends, HMS Stone director Beyza Baykan and her sister, as well as Zennure, meet us for some Tokyo denim vintage hunting and shopping. It was their first Tokyo trip, so we took them to all the best vintage shops and areas all around Tokyo including Koenji, which is one of my favourites, as well as stores like Kapital and BerBerJin. We were thrilled to also see our books at T-site Daikanyama, a 25-year denim career highlight!
July 6: Kojima, Japan We all take the bullet train to Kojima and spend five days at the world’s finest denim laundry, Howa. Did you know, Howa made the world’s first stone washing machine, based on a cement mixer, and it was still in use up until three years ago? What a shame we couldn’t use this machine for our book. They also did the first stone washing for Edwin, around 1976. We couldn't imagine doing a denim washing book without Howa’s involvement and were so excited they agreed to take part. We ended up creating 15 denim washes and I can honestly say, the Japanese have the best attention to detail. All of us really enjoyed Kojima as well, and saw the famous Jeans Street, where we might have been tempted to buy a few denim samples...
July 27: Venice, Italy Thankfully, we are at home for about 10 days after Japan, but it’s soon back to Italy, this time to Venice and Zaitex Laboratory, where we washed a further 10 garments with Garmon creative director Davide Vagnetti. These washes are truly superb and we can’t wait to show them in the book.
August 2: Istanbul, Turkey Home for 48 hours, then back on the plane for the final leg of the ‘Born to Fade’ project. We meet Zennure and wash 15 more garments at Kaiser in Istanbul using CleanKore’s resource-saving dyeing technology. We filmed with Beyza and her wonderful father at HMS’s factory, as we are creating content to show the benefits of using HMS stones, and visit Ereks Blue Matters to interview designer Beril Karabiyik, who helped us create all 75 garments for the project.
August 17: Karachi, Pakistan I consult for many denim mills each season, from designing collections to film and marketing story-telling work. This season I’m working with the wonderful Artistic Milliners on a secret project, which will be announced by the time you read this.
Late August: UK 22 INSIDE DENIM
We managed to enjoy the final part of the UK heatwave, ahead of the release of our latest book, ‘Endrime Presents: How to make a pair of selvedge jeans’. Over the summer we have also been slowly creating a downloadable digital denim pattern archive on our webstore.
September-October: Home, England Time to stay on solid ground for a short time. But no rest for the wicked, time for editing copy, colour-correcting, editing videos and translating for our numerous denim publishing works... Wish us luck!
APPLE STORE
GOOGLE PLAY
JEAN GENIE
Leanne Jae, denim design and wash innovation consultant, on why chemistry can unlock creativity, where denim finishing is heading next, and why the future of denim lies in experimentation, transparency and getting closer to the making.
The art of the wash
24 INSIDE DENIM
Q What drew you more deeply into wash chemistry when most designers tread cautiously around it, and what have you learned that’s made you a better designer? A I respond to “noes” with “why?” It’s how my brain is wired – curiosity has always been the thing that keeps me activated and engaged, and the biggest noes in my career were always in wash and chemistry. As a creative, the idea of learning about chemistry felt scary, daunting and not what I would consider a natural talent. My secondary school science teacher would be in utter disbelief that I chose to go all in of my own free will! But the more I learned, the more inspired — and honestly, the more annoyed — I became. Annoyed that I’d allowed myself to be intimidated by something that actually holds the key to being far more creative than I’d ever conceived. I walked past chemistry booths at trade shows for over 10 years, too daunted by the idea of feeling stupid. The reality is, whenever you ask someone why, you’re almost always met with a huge smile. People want to share what they know. That frustration led me to do something most designers don’t: I helped set up and now run London’s first sustainable denim wash R&D lab at Blackhorse Lane Ateliers, nearly five years ago. I was trained by the team at Tonello, one of the world’s leading wash technology innovators, and I’ve been running the lab ever since. Going into that world properly — understanding the machinery, chemistry and physics of what actually happens inside a wash cycle – didn’t make me less of a designer; it gave me a 360 view of the entire process so I could understand how to unpick and redo it. Looking back, I now see that design has become less playful. The scramble to hit the next trend, turn around the next collection, move faster and faster. We’ve become machines ourselves, which is deeply ironic given how much we talk about resisting automation. The play element – genuine creative exploration, the happy accident, the afternoon spent just trying something to see what happens – is largely gone from mainstream fashion development. I lost some of my love for design because of it. And I found it again, unexpectedly, through washing with my own hands.
Leanne Jae is an independent denim design and wash innovation consultant with 18 years of experience across luxury, heritage and fashion-led brands. Through her London-based consultancy, she works with brands at the intersection of creative direction, wash chemistry and sustainable development. She runs London's first sustainable denim wash R&D lab at Blackhorse Lane Ateliers. Her work spans design consultancy, industry workshops and innovation research. ALL PHOTOS: LEANNE JAE
What are the most common and costly mistakes brands make in denim wash development, and at what point could expert input save the most time and money? Fabric selection. In my experience, that’s where most mistakes happen and where the most time and money is lost. Denim has a raw state that a surprising number of brands – even established ones moving into the category for the first time – don’t fully account for. My favourite example was a client who handed me a Pantone reference and asked me to wash down to it. It’s a wonderful moment because it tells you everything about where the knowledge gaps are, and I say that with complete empathy; I was that person once, too. The challenge usually runs in one of two directions. Either a brand falls in love with a fabric and brings a wash target to it that the fabric simply cannot achieve – wrong construction, weight, indigo depth, etc. Or they have a beautiful wash vision and choose a fabric that will never get them there. Denim doesn’t work like other categories. You tend to need to work backwards – fabric first, wash target second. The fabric unlocks or closes down your creative options before a single garment is developed. The most costly moments in development often happen because fabric, wash and design are treated as three separate conversations rather than one. A designer knows what they want it to look like. A fabric technologist knows the cloth. A laundry knows the wash. When those three don’t talk to each other early enough, you get compromised outcomes, wasted sampling rounds and expensive rework. It’s not anyone’s fault, it’s just how the process tends to fragment. Flexibility matters more than people expect. Some of my best work has come from an outcome I wasn’t aiming for. Denim rewards a willingness to follow what the fabric is telling you rather than fighting it toward a predetermined target. A recent jacquard development is a good example. The design had an extraordinary level of shrinkage – not even uniformly across warp and weft – which meant we had to wildly distort both the print and the base pattern before a single thread was woven, just to accommodate what the wash would do. When the only samples came through, I washed them myself, which was terrifying as there was no back-up. It worked, but only because the fabric and wash knowledge was there from the beginning. Without it, the samples would have come back unwearable and the design unrecognisable.
JEAN GENIE What’s genuinely exciting in wash and surface technology that brands aren’t paying enough attention to? There’s a lot happening right now. Printed denim fades are gaining interest because they eliminate water-intensive washing and avoid unsustainable chemistry. I understand the attraction, and the environmental logic is sound, but I think the need for washing will continue, both for aesthetic reasons and because there’s something irreplaceable about what water, chemistry and mechanical action do to denim. Laser technology continues to evolve too, and I think it remains underutilised as a creative tool. The ability to extract wear patterns from vintage references, manipulate surface texture and create effects that previously required water-intensive chemistry is extraordinary. I use it regularly in my lab and the creative possibilities continue to surprise me. Combining laser with emerging chemistry is where some of the most interesting development is happening. Machinery innovation continues to advance – systems that recover indigo at near-zero wastewater discharge are increasingly viable at scale. AI is beginning to play a role too; Jeanologia has been using it to extract washing templates from photographs, which I think we’ll see more of. Measuring impact accurately is where I think the industry still has work to do. Some reporting tools rely on operator-inputted data, which introduces subjectivity and inconsistency. Tools that gather data directly from machinery, like METRO, developed by Tonello, are a much more reliable model. I’d love to see an industry-wide measurement infrastructure that works across all machine manufacturers, pulling data directly from equipment to give an accurate, standardised picture of water, steam and energy consumption per process. For me, though, the most exciting and underexplored areas remain chemistry and alternative fibre. I’ve been studying bio-engineered and bacteria-based dyes as a replacement for synthetic indigo; companies like Pili, whose fermentation-derived indigo has the same molecular structure as conventional indigo, are doing groundbreaking work that could fundamentally change how we colour denim at yarn stage. We’re also seeing bio-based alternatives to conventional elastane emerging, and cotton grown regeneratively is starting to make its way into the supply chain. The thread connecting all of these for me is that the most exciting innovations aren’t about making the existing process slightly less bad. They’re about rethinking the inputs entirely – what we dye with, what we weave with, where it comes from. That’s where I think the real leap forward is.
25 ISSUE 18 / 2026
Leanne with Andrea Vernier and the Officina39 team in Italy.
JEAN GENIE 26 INSIDE DENIM
Where is denim and textile development heading in the next five years – what’s coming that most people haven’t seen yet? AI will continue to transform the entire denim supply chain, from intelligent farming and soil health measurement through fibre and weave development, all the way into dyeing and washing. We’re only at the beginning of understanding what that could mean for precision, consistency and waste reduction. But here’s what I think people aren’t seeing clearly enough: as AI becomes more embedded, the human touch is going to become more celebrated, not less. There will be a growing appetite for handicraft, artisanal technique and the visible hand of a maker. Those two things will coexist, and I think the most interesting denim of the next five years will sit at exactly that intersection: technology enabling craft rather than replacing it. On the regulatory side, digital product passports are coming and they’re going to force a level of transparency that most brands are simply not prepared for. Every garment will need to tell its full story: fibre origin, dye chemistry, water consumption, manufacturing location. That’s not just a compliance challenge, it’s a creative opportunity for brands that have genuinely good stories to tell. REACH chemical restrictions in Europe are already forcing the reformulation of finishing chemistries, accelerating the shift toward bio-based alternatives. Equally significant is Extended Producer Responsibility legislation for textiles. EPR will require brands to fund the reverse supply chain for their products, from waste management through to resource recovery. Europe is moving faster here than the UK, which does not yet have formal EPR legislation for textiles. But it’s coming, and when it does, it will fundamentally reshape how brands think about product design, material selection and end-of-life. The infrastructure challenge I think about most is water recycling at scale, at a price point accessible to factories anywhere in the world. Closed-loop water systems exist and they work, but remain out of reach for much of the global manufacturing base. If the industry could solve that access problem, we would fundamentally change the environmental footprint of denim production globally. That’s the breakthrough I most want to see in the next five years. Is truly sustainable wash development achievable at commercial scale or are we still largely greenwashing? I have just spent three days in Italy working on exactly this problem, trying to develop sustainable washing at commercial scale that is cost-neutral for a high street brand. The honest answer is: it costs more. Not dramatically more in every case, but more. What I’ve learned is that the most realistic and impactful route right now isn’t a wholesale overnight switch to green chemistry. It’s a transitional approach: strategically blending established chemistry with emerging sustainable alternatives to progressively reduce environmental impact while keeping the cost equation workable. That’s not a compromise on ambition. That’s how systemic change actually happens. The bigger problem, in my view, isn’t what’s happening in the lab. It’s what’s not being communicated to the end consumer. If a buyer knew exactly what chemicals were sitting against their skin in a pair of jeans – the potassium permanganate, the softeners, the finishing agents – would they make different choices? I think many would. But we give them almost no information to make that decision with. We’ve made extraordinary progress as an industry. But progress without transparency doesn’t create consumer demand for better product. And without that demand, brands have limited commercial incentive to invest in change beyond what legislation requires.
There’s something about the physical connection between maker and material that reawakens the creative instinct. What I’d love to see, and what I think is coming, is a standardised visual communication system for garments. Something like the traffic light nutritional labelling on food packaging. You don’t need to read the ingredients list to understand that something is high in sugar, you see the red label and you know. Garments need an equivalent. How do you hold the creative and technical together – does one ever win over the other? Honestly, there is some tension between them, and I don’t think it ever fully disappears. Creative intent and technical possibility aren’t always aligned, and when they’re not, something has to give. Most of the time that’s expensive – in sampling rounds, time and compromised outcomes. The reason I went so deep into the technical side wasn’t to become a technician, it was to reduce that mismatch. To be the person in the room who can say "that won’t work, but this will" before anyone has spent money finding out. But sometimes the mismatch produces something extraordinary. And knowing the difference between a risk worth taking and one that isn’t, that only comes from being close to the making. There’s something about the physical connection between maker and material that reawakens the creative instinct. Standing at a machine, watching a fabric transform, not knowing exactly what’s going to come out – that’s play. That’s where the unexpected happens. The distance between designer and product has grown to the point where it mirrors the distance between product and buyer. Both are too far removed from the making. If designers were closer to the process and consumers were closer to the story of how something was made – what went into it, what it cost the planet to produce – I think both the creative output and the purchasing decisions would be fundamentally different. A client came into the lab with a linen suit. They wanted to laser it. I’d just watched a vintage jacket catch fire on the laser bed because I’d missed a label, so my instinct was a firm no. But they kept pushing. Eventually I agreed to test on a sample they didn’t need. It didn’t go wrong. It came out beautifully. We extracted a laser wear pattern from a sun-faded original sample, edited it together, and a few weeks later that linen suit was walking down a catwalk. That’s the balance. You need to push, and sometimes you need to be pushed. The technical knowledge tells you where the real risks are – which means you can take the creative risks more confidently. That’s where the magic happens. Not in choosing one over the other, but in knowing both well enough to know when to listen to each.
DETOX
Game changer for Indigo Dyed Denim. Hydrosulfite and Aniline free. Nature Conscious Dyeing
by BluConnection. Your trusted and reliable partner.
SCIENCE BEHIND THE FADE
The distressed denim dress that inspired Gap to create a custom gown worn by K-pop star Ejae. ALL PHOTOS: WTP
The only full-service denim laundry on the East Coast of the United States, BPD Washhouse has carved out a unique creative and commercial niche for brands large and small. Its uniqueness extends to an openness to exploring new ventures, and training tomorrow’s denim professionals, a mission dear to founder Bill Curtin.
Connections & creativity drive BPD Washhouse
28 INSIDE DENIM
M
aking connections is what makes Bill Curtin tick. The close-knit network he has built up over the years has shaped his career in textiles and denim, leading ultimately to the creation of Blueprint Denim (BPD). He took his first steps in the industry working for a textile converter, which, in hindsight, placed him squarely at the crux of the matter. He learned the art and craft of denim and washing through stints working for the likes of Levi Strauss, Calvin Klein, Tommy Hilfger and Converse. When the American jeans industry was transferred off-shore, he travelled extensively, expanding his connections globally. Among these, a Chinese entrepreneur working for Décor Global would provide the financial backing he needed when he took the decision to establish his own business. BPD Washhouse was founded in 2009 with the acquisition of a facility owned by Jones New York (now part of the One Jeans Group). Located in Jersey City, just across the Hudson River from Manhattan, it is now a small but powerful cog in the wheel of America’s fashion capital.
“We are the only full-service wet and dry process facility on the East Coast of the United States,” Bill Curtin likes to say. He admits that “there are others in and around New York that can do some processes, but we are the only ones to cover all dry and wet operations in house.” These include garment washing and lasering as well as a newly bought ozone device, as well as a newly bought ozone device from Jeanologia. Garment dyeing is also part of the picture, and a growing activity for the company. “We are seeing a big push for colour in denim, and knits,” he says.
A multi-facetted operation “Our plan from the start was to create a multi-platform business,” he points out. While product development for large and small brands and designers is the washhouse’s main business, it also welcomes special projects for TV shows, Broadway musicals, ballet companies, and urgent day-before-show requests from fashion designers. A high point of 2025 was making a custom denim dress for Gap that was worn by K-pop singer and songwriter Ejae at the 2025 CFDA Fashion Awards in New York City. Zac Posen made the trip to Jersey City and spotted a dress on display in the showroom that inspired him. He had already chosen a fabric, which Bill Curtin said would not withstand laser treatment. The gown’s panels had to be dremelled by hand. “It took a whole week, was way over Gap’s initial budget, but the dress received huge media coverage.” The facility is not big enough for industrial production, but it can produce short runs for designers. Its main activity is developing recipes for brands, such as those of the Knitwell group, which includes Loft, Ann Taylor, Chico’s and Lane Bryant. When Inside Denim visited the facility, a team from Telfar was on site. The laser and ozone machines are used for development purposes to set the parameters for industrial production. With shrinking travel budgets, Bill keeps an eye on production runs at factories in Asia via WhatsApp. Spreading knowledge Getting the right product to market works best when there is a common language between the design and product team and laundry staff. BPD addresses this with its well-known denim classes. These are open to its customers’ staff whether they are denim specialists or not, like when a knit design team is looking for special washed effects. “Denim finishing has its own language, which insiders usually to keep to themselves, and English is often a second language for people in production,” he points out. Any misunderstanding can quickly lead to a botched production. “The washhouse guys can tell if a production manager knows what they are talking about. If a 50% change in a fade is requested, at the production stage, that is akin to creating an entirely new product. And if a 5% change is desired, the washhouse may decide to dismiss the request.” He recommends using simple language, without modifiers. “When both parties understand each other, it breeds confidence and trust.” Bill Curtin has recently decided to expand his knowledge sharing mission to chemistry by creating closer connections with chemicals companies. “The chemical side of washing can be the most intimidating,” he says. He has set up a partnership with Near Chimica, from Italy, whose team comes to Jersey City to train both the in-house BPD team and customers. This partnership allows designers to discover new product ranges and deepens their sustainability skills. The evolution of processes, like replacing pumice stones with enzymes, can lead to major savings in energy and water, he stresses.
SCIENCE BEHIND THE FADE
Encouraging more sustainable practices is fundamental to BPD’s ethics. “We have three pillars of sustainability: one is the earth, keeping the environment clean; two is ethical working conditions; and the third is economics. If something is not economically feasible, it’s not going to work.” Bill Curtin sees promise in new potassium permanganate alternatives and expects PP to be phased out in the next five years. In time, he expects alternatives to bleach to become standard as well. “It is a step-by-step process. Like integrating preferred fibres, it is best to start small. There is no valid reason to make a 100% post-consumer recycled jean that no one will want to buy.” New blue blood Over the past few years, Bill Curtin has surrounded himself with a staff of young professionals. Charlie Cutt, in charge of lasering and trained at the Parsons School of Design, has been with the company for just over a year. Project manager Kelly Schliefer was recruited three years ago, after an internship during her studies at FIT. Bill spotted Bryan Morales’ talent for sanding when renovating his own home. Three years ago he hired him to work on fades, whiskering, and all dry and wet techniques. “The kids are not held back by tradition, they know digital design tools, and they get sustainability,” says Bill. They are in essence the blue blood that will build their own connections and shape tomorrow’s denim industry.
Bill Curtin founded Blueprint Denim Washhouse in 2009.
29 ISSUE 18 / 2026
The washhouse’s proximity to New York City and its fashion ecosystem makes creativity essential to its ongoing success. “We turn any idea a designer has in mind into a finished item,” Bill Curtin tells Inside Denim. In whatever form these ideas come, a prototype, a conceptual design, a few photos or a mood board, BPD translates even the most abstract directions into physical products. The house’s creative touch has attracted high profile names such as Coach, Alexander Wang, Telfar, and even Marc Jacobs.
FACTORY TALK
An example of a coloured weft made by Santanderina. ALL PHOTOS: TILMANN WRÖBEL
No guts, no glory!
30 INSIDE DENIM
I
drove from my office in Biarritz to Cantabria, a region bordering the Basque country, to visit Santanderina, whose factory is located 20 minutes away from the port and city of Santander. Like Bilbao, the historical industrial port is now turning into a cultural tourist destination. Did I mention a rich industrial history? Textil Santanderina has a long and rich history. The company was founded in 1923 by a family from Santander that still owns the business. As often in our industry, true family affairs have a different flavour and taste; a very different take on business compared to private equity. Deliberately, I use the term company, as Textil Santanderina’s is more than a denim mill. Its yearly sales of €90 million come from several activities. The ready-made garment sewing unit accounts for 5% to 10% of its revenues. The remainder is generated by the mill’s fabric production that addresses two markets. Technical workwear fabrics, textiles that are fire retardant, resistant to chemicals and such, make up 50% of its sales. The other 50% are sales of fabrics for fashion, otherwise known as flats and denims. These are the mill’s iconics. They include lightweight, super soft feminine fabrics, in plains or prints, and denim fabrics, at times blended with Lenzing’s Tencel lyocell fibre.
FACTORY TALK: TEXTIL SANTANDERINA It has become near mandatory for fabric mills to focus their efforts on potential best sellers, commercial weights, casts and constructions, those that hopefully correspond to what a ‘mass’ consumer might expect from their jeans. There are, however, mills that boldly go against the current and present fantastic, creative and powerful fabrics with a strong identity and character. Textil Santanderina is part of that ‘guts and glory’ breed. On the factory floor Once entering the factory, one can see the traces of old train rails, which delivered the cotton bales straight into the factory a hundred years ago, and also new machinery of the finest make. From ginning, spinning, dyeing, weaving and to finishing, the factory is vertically integrated. Thanks to the versatile machinery, company engineers can spin the perfect yarn needed for specific technical fabrics or cool denim. A beautiful slasher dye and a variety of modern shuttle looms, for slower, looser weaves, and faster air pressure looms, fill the huge weaving hall.
FACTORY TALK Founded in 1923, Textil Santanderina is a family-owned business based in Cabezón de la Sal, Cantabria.
That meeting between Isabel Marant and Santanderina inspired the mill’s teams to develop big and bold denim fabrics, leaving aside the more common commercial stuff that most other denim mills repeat and repeat in their offerings. Laura Torroba, the head of design, then started digging deep into the Japanese denim and workwear culture and after a while brought up this fascinating range of fabrics. Sashiko-fabric double indigos, huge rugged rings, bold crosshatches. Hairy felt-type denim fabrics. All in very thick yarns, loose weaves, delivering that very modern gender fluid, soft, yet chunky and authentic denim flavour. Some of these fabrics are available prepared-for-dyeing (PFD), which opens more space for creativity. All the more so for designers in love with the ‘future archaic design’ movement. Currently Santanderina is presenting this creative fabric range to upmarket and luxury brands, and I cross all my fingers, that this brave and bold approach to fabric development will lead to our much needed and precious oxygen benchmarks. Oxygen that will bring freshness to denim in general, to our industry, to denim design. And that the mill will successfully pull this off. I congratulate Santanderina for embarking on this daring “wow” move! You are real makers!
Tilmann Wröbel is the founder of Monsieur-T, the ‘denim lifestyle’ studio. He started his career as a haute couture designer before moving into streetwear and denim. He has worked as a designer and consultant for some of the world’s top brands. He is based in Dusseldorf, Germany, and Biarritz, France. MONSIEUR_T_OFFICIAL PHOTO: CHRISTIAN GEYR
The mill’s slasher indigo dyeing line.
31 ISSUE 18 / 2026
Santanderina’s creative team is led by Laura Torroba, who is based in Barcelona, and keeps a close eye on the latest fabric trends. A detail worth noting. Let me tell you how I (re)discovered Santanderina’s fabrics. At Kingpins Amsterdam last April, with my client A.P.C., I eyed a rack with unusual fabrics of great character and interest. As I was pointing out these heavy, loose and creative Japanese-type fabrics to the A.P.C. team, I realised that I was standing on the Santanderina booth, with Ramón Ríos Quintana (the boss) and Laetitia Grimoult (the sales director) standing next to me. Big was my surprise to be handling not Santanderina’s usual soft, silky thin women’s denim, but truly bold and singular denim fabrics woven with extra thick yarns, sporting strong Japanese-type loose-weave or hairy vintage denim textures. I have to admit that it has been a while since a European mill development impressed me. There are still a few fantastic denim creatives in Italy, Turkey, and Japan, of course, who have a more individual approach to denim fabrics, to the extent that the real ‘gems’ are rarely shown. I asked if I could come to Santander, to see, feel and understand the story behind these bold developments, which I felt in love with. Once there, I learned that these special developments were slowly initiated in 2023. They were the result of a meeting with French designer Isabel Marant, who was looking for extra heavy yet drapey denim constructions. Having worked closely with Isabel some time ago, I know well how deep and passionate her approach and knowledge of Japanese denim is.
CLOCKING ON...
CLOCKING ON... For CleanKore’s technical director, Anu Wijesooriya, every day is about people, collaboration and purpose – balancing customer meetings, lab development, and brand, mill and laundry relationships to drive sustainable denim forward.
Purpose in every process Anu Wijesooriya is a technical director at CleanKore. A textile engineer with a BSc from Sri Lanka and an MBA from the UK, he has spent nearly 25 years in the denim industry across Sri Lanka, Bangladesh, India, China and the Philippines. His current role spans washing, lab testing, costing and end-to-end technical support for CleanKore developments. PHOTOS: ANU WIJESOORIY
I want to share a normal day in my life when I am working with my supply chain partners in Bangladesh. I travel at least once every month to Dhaka, which was also my home base when I was previously helping to lead the innovation team at Kontoor’s Bangladesh operations.
6:00am I like to start early. Quiet time in the morning helps me think clearly, check overnight emails from different time zones and prepare for the day’s visits, trials and meetings.
8:30am Morning meeting with brand customer to review hangers, development priorities and ongoing CleanKore styles. We now have 16 international customers in production, with many of these customers having garmenting or fabric production in Bangladesh. I work closely with Shakeb, our Bangladesh-based CleanKore wash technician, to ensure we support our customers at every technical step.
10:30am Another brand meeting focused on recent laser brightness testing (LBT) where we discuss results on how different intensities of laser (or hand sanding) can help them to achieve the right look, feel and performance while keep production efficient and sustainable.
12:30pm Mill visit and meeting with their marketing team. We discuss how to co-market, work on their existing fabric to convert to CleanKore fabric and provide other options that add value: better stories, better products and stronger sustainability credentials for our mutual customers.
32 INSIDE DENIM
1:30pm - 5:30pm Travel to our laundry partner and work with their team. This is where ideas turn into real solutions! With Shakeb and the laundry team, we focus on lowering steps and leaning out wash recipes while still achieving the look without PP spray or alternative chemicals and boosters. We make sure to hit the design and sustainability goals without increasing full package garment costs!
7:30pm - 9:30pm Meet up with ex-colleagues and friends. Great dialogue, honest conversations and sharing industry knowledge keeps us all growing. The denim community is built on trust, respect and helping each other succeed.
10:00pm Call time with family! No matter how busy the day is, I always make time for my wife and kids. They are my strength and my “why.” Being a good husband and dad keeps me grounded, motivated and grateful every single day.
MAGAZINES ISSUE 18: 2026
BEHIND THE SEAMS OF THE GLOBAL DENIM INDUSTRY
ESTABLISHED 1987
THE WORLD’S NO.1 MAGAZINE FOR THE LEATHER INDUSTRY
VOLUME 32 ISSUE TWO 2026
Volume 39, Number 4
August / September 2026 | [Published 21st August 2026]
A mile in these shoes
The boot that won the World Cup Why Le Marche is still special Inov8’s move away from DTC
How Kocher & Levi’s created couture
A stretch for plant-based Performance beyond exercise Enter the enzymes
Le Marche: still special Alternatives for colour-matching Full FILK round-up Bangladesh seeks change
A magnificent mile Elasticity edges closer to nature / A trip to BPD Washhouse Art of the laundry / AI’s influence on design / Endrime’s epic journey
Inside Denim
Sportstextiles
Footwearbiz
World Leather
Keep up to date with denim developments from raw material to finished product with in-depth coverage of advances at fibre and fabric level. (2 issues per year)
The international technical trade magazine for innovative and responsible materials. (2 issues per year)
All you need to know to assist you in the global footwear market. (4 issues per year)
The world’s leading magazine for the leather industry. (6 issues per year)
Sportstextiles (Digital)
Footwearbiz (Digital)
£100 per year
Footwearbiz Premium (Print)
£140 per year
£100 per year
Sportstextiles Premium (Print) £120 per year
World Leather & Leatherbiz (Digital)
£270 per year
World Leather (Print) & Leatherbiz
£300 per year
Websites
To be kept up-to-date on what’s happening in the denim industry... sign up now.
Designed to provide up-to-the-minute news and market intelligence.
InsideDenim.com is the news portal to complement Inside Denim® magazine, offering the latest industry news, market intelligence, product information and much more. It is a comprehensive news site for the industry, which boasts a searchable archive of stories, as well as emailed newsletters and a technical online library of Inside Denim® articles.
ORDER FORM
50% OFF
The must-have essential book for the footwear designer
_ £69 £34.50
From materials through the stages of design and production To place an order, send your enquiry to john@worldtrades.co.uk