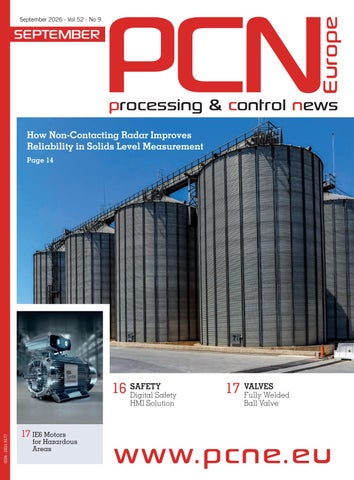
September 2026 - Vol 52 - No 9
SEPTEMBER
How Non-Contacting Radar Improves Reliability in Solids Level Measurement Page 14
16 SAFETY Digital Safety ISSN : 2031-9177
HMI Solution
17 VALVES Fully Welded Ball Valve
17 IE6 Motors
for Hazardous Areas FREE DIGITAL SUBSCRIPTION
002_017_IEN Europe_September 2026.indd 13
N° 9 - SEPTEMBER 2026
04/09/26 14:13
14 measurement&instrumentation How Non-Contacting Radar Improves Reliability in Solids Level Measurement Advanced non-contacting radar technology addresses the challenges of solids level measurement – helping to eliminate costly maintenance and downtime, as demonstrated in a recent waste-to-energy application. Automation has significantly improved safety, efficiency and productivity in the process industries, yet further performance gains are possible. Unplanned downtime still affects overall equipment effectiveness, with lost production and maintenance costs impacting profitability. While pumps, motors, fans and compressors are often viewed as the main risks, process automation and measurement instrumentation are equally critical. Improving the reliability and long-term performance of field devices is therefore essential. These instruments often operate in harsh environments, facing extreme temperatures, pressure, corrosive materials, vibration and dust. Bulk solids applications are particularly challenging. Challenges Measuring solids is far more complex than measuring liquids. Unlike liquids, which form a flat surface, solids create uneven profiles, adhere to vessel walls, and change shape during filling and emptying. Ratholing can leave material along the walls, causing operators to overestimate available capacity and increasing the risk of overfills. These conditions affect signal reflection and measurement accuracy. Reliable level measurement therefore requires technologies that can cope with uneven surfaces, unpredictable flow patterns, and low-dielectric materials that provide weak signal reflections. Dust Generation Significant amounts of dust can be generated during solids filling and discharge. In sufficient concentrations, airborne dust can present serious respiratory hazards and reduce vis-
002_017_IEN Europe_September 2026.indd 14
Typical ash storage tanks offer a difficult monitoring environment with uneven surfaces, fast filling and a high level of dust. Picture: shutterstock_1454277722
ibility. Many dusts are also combustible; when combined with oxygen and an ignition source, dust clouds can lead to flash fires or explosions. Even minor overfills or uncontrolled discharge can increase dust concentrations, raising the likelihood of ignition from static electricity, hot surfaces or mechanical sparks. Dust and electrostatic charges can also affect level measurement accuracy and reliability. High dust concentrations may attenuate signals, create false echoes or lead to build-up
on sensor surfaces. Over time, this can result in signal loss or inaccurate readings, making robust instrument selection critical.
N° 9 - SEPTEMBER 2026
FREE DIGITAL SUBSCRIPTION
Equipment Overload and Structural Stress Solids can impose significant mechanical stress on vessels, handling equipment and instrumentation, increasing the risk of failure. Overfilling further exacerbates these forces, potentially overloading feeders, screw conveyors, rotary valves and discharge gates,
04/09/26 14:13
15 Rosemount 3408 Non-Contacting Radar Level Transmitters have been installed on the three storage vessels storing treated fly ash from the waste-to-energy incineration facility.
highlighting the need for reliable and accurate level measurement. Material movement during filling and discharge can also place physical strain on contacting measurement devices, affecting their reliability and service life. For example, the probes of guided wave radar level transmitters may be subjected to bending, tensile or dragging forces as solids shift and settle, increasing the likelihood of damage or measurement degradation. Benefits of Non-contacting Radar Non-contacting radar devices are well suited to a wide range of solids level measurement applications. They transmit electromagnetic signals that reflect from the material surface back to the antenna, enabling level measurement without physical contact. This makes them particularly effective in dusty environments and over long distances. Modern noncontacting radar transmitters based on frequency modulated continuous wave (FMCW) technology offer high accuracy and sensitivity, while requiring minimal wiring for power and communication. Advanced signal processing allows these devices to ignore false echoes from internal obstructions, ensuring reliable measurements. They can also accommodate uneven and constantly changing surface profiles caused by phenomena such as bridging and ratholing. Specialised solids algorithms enable a representative average level to be calculated across a broader surface area, rather than relying on a single-point reading. For highly dusty environments, air purging systems can FREE DIGITAL SUBSCRIPTION
002_017_IEN Europe_September 2026.indd 15
be used to prevent antenna build-up, maintaining signal strength and reducing maintenance requirements. Minimised Maintenance Requirements Modern non-contacting radar transmitters are designed for reliable, low-maintenance operation, helping to reduce downtime. Built to withstand shock, temperature extremes and outdoor exposure, they continue to perform in demanding environments such as silos, crushers and conveyors. Because the device does not come into contact with the material, there are no components exposed to wear, bending or damage from abrasive solids, heavy loads or vibration. This eliminates common failure modes associated with contacting technologies. Coating and build-up are also less problematic, as the antenna is positioned above the process and can continue operating even in dirty conditions. As a result, the need for cleaning and maintenance shutdowns is significantly reduced. With no moving parts, these devices offer improved long-term reliability while keeping maintenance requirements and costs to a minimum. Measuring the Level of Fly Ash A good example of how non-contacting radar has eliminated downtime in a challenging solids level measurement application can be found at a waste-to-energy plant in Europe. Compressed fly ash produced from the incinerator is used as a construction material in road building. After chemical treatment, the
ash is stored in three large (16 metres high) vessels ready for collection by trucks. The plant operator must continuously monitor ash levels to prevent overfilling, manage inventory, and schedule refilling, maintenance and cleaning when necessary. Monitoring fly ash levels is difficult due to uneven surfaces, fast filling, and a highly dusty environment. The ash tends to stick to surfaces, creating build-up within the vessel and on instrumentation. The company had been using guided wave radar devices from another vendor, but ash accumulated on the probes, causing clogging after five or six days and leading to unreliable measurements. Weekly maintenance was required to clean the probes, exposing personnel to dust and taking vessels out of service for up to two hours. This interrupted operations and reduced overall process efficiency. Emerson provided a replacement solution by installing a Rosemount™ 3408 Non-Contacting Radar Level Transmitter on each vessel. Key factors in the selection included ease of integration, fast commissioning and a strong return on investment. Although fly ash has a low dielectric constant, the FMCW technology used in the Rosemount 3408 maximises sensitivity to ensure accurate measurement. A smart solids algorithm enables reliable readings despite uneven material surfaces, while an advanced air purging system prevents antenna build-up. Signal quality diagnostics provide additional assurance by alerting operators to abnormal conditions or build up on the antenna. The transmitters have delivered trouble-free operation, eliminating unplanned stoppages and improving both treatment and loading processes. Increased vessel availability has enabled more efficient truck loading, resulting in annual savings of approximately $80,000 and a return on investment in just one month. 67028 at www.pcne.eu
N° 9 - SEPTEMBER 2026
04/09/26 14:13
16 HYGIENIC OVAL GEAR FLOWMETERS
AI-SUPPORTED PIPELINE MONITORING
More performance without changing dimensions
For continuous monitoring, leak and theft detection
Titan Enterprises has released a newly engineered design for its OG3 and OG4 oval gear flowmeter models. Designed for use in industries where cleanliness, accuracy and reliability are critical, the new flowmeters feature an electropolished stainless-steel finish that provides a smooth, easy-to-clean surface suitable for food and beverage, pharmaceutical, biotechnology, cosmetics and personal care manufacturing environments. A key advancement in the redesign is the transition from a cast body construction to a fully machined, engineered design. The precision-machined construction not only enhances mechanical strength but also supports the high levels of measurement accuracy and repeatability for which Titan's oval gear flowmeters are recognised. While delivering enhanced performance for hygienic processing applications, the models still maintain the original dimensions of the previous oval gear products to allow interchangeability within customers' existing systems. The new OG flowmeter design with Hall effect detection, also benefits from an upgraded circuit board with added protection from mis-wiring or electrical surges, as well as offering both NPN and PNP outputs as standard (up to 100°C max). The OG3 and OG4 flowmeters provide precise volumetric measurement of liquids across a wide viscosity range.
Krohne introduces PipePatrol NEO, a new comprehensive solution for leak detection, theft detection and pipeline monitoring. The core of the system is the NEPM (Neural Engine Pipeline Monitoring) next-generation technology for continuous internal pipeline monitoring. It combines artificial intelligence with proven physical models, providing an effective way to manage the complex risks of modern pipelines - from corrosion and equipment failure to third-party interference, illegal tapping, and environmental impacts. It is designed for a wide range of applications, including oil and gas pipelines, chemical processes, water and wastewater networks, as well as district heating and hydrogen infrastructure. PipePatrol NEO applies NEPM, an AI-enhanced multi-method approach which integrates advanced hydraulic modelling, statistical pattern recognition and real-time measurements of flow, pressure and temperature. By continuously comparing a "virtual pipeline" model with actual operating data, the system detects deviations and analyses them using AI-based pattern recognition. It continuously learns from operational data, adapts to changing conditions and delivers precise, reliable pipeline information in real time. This enables faster detection, highly accurate leak localisation and minimal false alarms, even under complex and transient operating conditions.
67027 at www.pcne.eu
67020 at www.pcne.eu
DIGITAL SAFETY HMI SOLUTION
12-PORT-ETHERNET-APL SWITCH
For functional safety in accordance with IEC 61508
Compact design with approvals for worldwide operations
The certification of the Deuta IconTrust® HMI confirms that the system can display safety-related data up to SIL 3 and process safety-related touch inputs up to SIL 2. The digital human-machine interface - IconTrust® HMI - is designed for safety-related display and control tasks. This globally unique SIL3 solution is certified to EN 61508 and offers 'Security by Design'. The solution is particularly relevant for applications where functional safety, traceable process versioning and efficient adaptability to changes throughout a plant's lifecycle come together. In many process industry plants illuminated panels, switches and individually wired signals are still in use. Whilst these have long proved their worth, they quickly reach their limits when changes, maintenance or retrofitting are required. IconTrust® HMI transfers these tasks to a digital interface. Safety-related display and control elements can be created there via a web-based configuration and adapted to specific projects. Useful information for day-to-day operations can be made available digitally, without any loss of time caused by working with analogue manuals. The system is designed as a PROFINET/PROFIsafe field unit and is used as a fixed-location safety control unit. The PLC remains in control: the safety controller determines which information is displayed securely through independent monitoring of the defined display areas.
Phoenix Contact is expanding its Ethernet-APL portfolio to include two managed switch versions with twelve ports for process automation. The Ethernet-APL switches enable the two-wire Ethernet connection of devices and sensors in the Ex zones of process technology applications. This allows sensors and devices from the field level to be connected directly to the system's Ethernet network. The data from the field level can be used in real time for process control, monitoring, and diagnostics. The devices feature optimized firmware user guidance for intuitive configuration, simple startup, and improved diagnostic functions. Their compact, lightweight design enables space-saving installation and in-line mounting in the control cabinet. With support for Ethernet-APL power class A, the switches provide an efficient power supply for field devices. In addition, both versions are approved worldwide and can therefore be used globally in applications for potentially explosive areas. The twelve-port switches help customers use Ethernet-APL in a wider range of greenfield applications - particularly in the chemical and pharmaceutical industries, marine and offshore applications, oil and gas applications, mining, and biomass plants, including demanding Ex environments.
66988 at www.pcne.eu
66944 at www.pcne.eu N° 9 - SEPTEMBER 2026
002_017_IEN Europe_September 2026.indd 16
FREE DIGITAL SUBSCRIPTION
04/09/26 14:13
17 2G MIGRATION FOR THE WATER INDUSTRY
IE6 MOTOR FOR HAZARDOUS AREAS
Modernise existing installations with reduced investment
Certification to ATEX and IECEx for global deployment
In view of the upcoming shutdown of the 2G mobile network in Germany, Panasonic Industry and INSYS icom are combining their expertise to support operators in the water and environmental sectors with the migration to future-proof communication solutions. Deutsche Telekom plans to shut down its 2G network by no later than June 30, 2028, in order to free up frequencies for more powerful technologies such as 4G (LTE) and 5G. Without timely migration, outages may occur, as devices that only support 2G will no longer be able to establish network connections after the shutdown. Existing systems must be migrated to future-ready technologies in good time to ensure long-term operational reliability. At the heart of the solution is Panasonic Industry's FP-I4C communication controller, combined with industrial routers and gateways from INSYS icom. The FP-I4C enables existing serially connected controllers to be integrated into modern networks without requiring a complete system replacement. This retrofit strategy not only helps companies reduce costs but also supports sustainability by extending the life of existing hardware. By migrating to modern mobile communication technologies, companies benefit not only from higher bandwidth and lower latency but also from enhanced security mechanisms.
ABB offers an IE6 Hyper-Efficiency motor certified to ATEX and IECEx requirements for use in hazardous areas. The new IE6 Increased safety motor, based on ABB's magnet- and rare earthfree synchronous reluctance (SynRM) technology, offers up to 60 percent lower energy losses than the IE3 induction motors commonly used in Zones 1 and 2. This enables operators to realize a major boost in energy efficiency and avoided carbon emissions in industries where gas, vapor or dust might be present, such as chemicals, marine, oil & gas, pharmaceuticals and food & beverage. The IE6 SynRM Increased safety motor is certified for use with variable speed drives (VSDs) to offer accurate control and high efficiency throughout the whole speed range, even at partial loads. The new IE6 SynRM Increased safety motor covers ratings from 110 kW, with IE5 versions available for up to 90 kW. As well as increased reliability and reduced maintenance, SynRM technology enables a more cost-effective installation. In Zone 1, cooler running can allow the use of an Increased safety SynRM motor where a Flameproof motor with a special enclosure would be the traditional choice. Furthermore, in Zone 2, the improved loadability of SynRM motors enables more power from the same size as an equivalent induction motor. This could enable a smaller, lower-cost motor to fulfil the same duty.
67017 at www.pcne.eu
66872 at www.pcne.eu
COMPACT RADAR LEVEL SENSOR
FULLY WELDED BALL VALVE
Continuous measurement in a range of up to 100 °C
Floating or trunnion ball design for critical infrastructures
WIKA has expanded its level measurement portfolio with the addition of the ILT radar sensor. The free-beam sensor enables non-contact level measurement, even through the walls of plastic containers. Its compact design makes the ILT particularly suitable for applications where space is limited. Manufacturers can, for example, install the sensor in mobile working machines or heating systems. Furthermore, non-contact technology enables high-precision measurement of the level of particle-containing, highly viscous or solid materials. Possible applications range from wastewater plants to all types of raw material containers and fuels. The ILT-C01 version is designed for a temperature range of -40 to 100 °C, while the ILT-C05 version also covers high temperatures up to 150 °C. Metal shielding protects the sensor from interference caused by electrical fields in the environment. The instrument operates reliably even under adverse conditions such as dust, moisture and heat, and can tolerate vibrations and shocks of up to 100g. With up to two additional switch points, further switching outputs can be integrated, for example for overflow or dry run protection. Last but not least, the radar sensor ensures low operating costs, as it is maintenance-free thanks to its non-contact measuring principle and wear-free design.
VIS VANA has developed its Fully Welded Ball Valve series to meet expectations for higher levels of safety, reliability and lifecycle performance in transmission pipelines, district heating networks, power plants, LNG terminals and other critical industrial applications. The fully welded body design eliminates potential external leakage paths while significantly increasing structural integrity. It also reduces maintenance requirements and improves resistance against vibration, thermal expansion and external mechanical loads. The valve is designed in accordance with API 6D and can be supplied in pressure classes ranging from ASME Class 150 to Class 2500, with sizes extending to DN1200 (48") depending on project requirements. Various body materials including carbon steel, stainless steel, duplex and super duplex stainless steels are available for corrosive and severe service environments. According to operating conditions a floating or trunnion-mounted ball design can be selected. Soft seated and metal seated configurations are available, enabling reliable shut-off in both standard and high-temperature applications. Fire-safe construction, anti-static devices, double block and bleed functionality, emergency sealant injection systems and stem extension options are available.
66967 at www.pcne.eu FREE DIGITAL SUBSCRIPTION
002_017_IEN Europe_September 2026.indd 17
67015 at www.pcne.eu N° 9 - SEPTEMBER 2026
04/09/26 14:13