THE V O L U M E
6 0
•
I S S U E
3
O C T O B E R
2 0 18
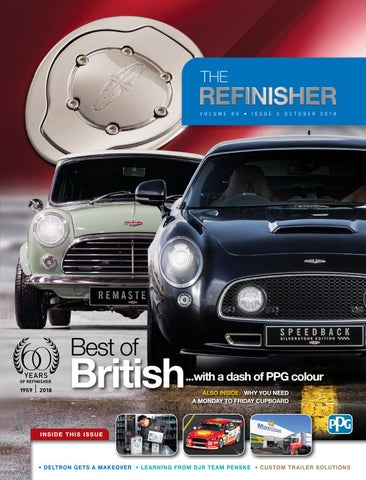
Best of
British
...with a dash of PPG colour ALSO INSIDE: WHY YOU NEED A MONDAY TO FRIDAY CUPBOARD
INSIDE THIS ISSUE
• DELTRON GETS A MAKEOVER • LE ARNING FROM DJR TE AM PENSKE • CUSTOM TR AILER SOLUTIONS
TOP OF THE CL ASS
Packed with advanced global technologies, specially tuned to local conditions, the popular DELTRONÂŽ refinish system sets the benchmark for solvent-borne performance. Featuring a tried and true reputation for ease-of-use, reliability and impeccable finish, the expanded array of primers and clearcoats are formulated to achieve outstanding results in almost 13 24 24
@PPGANZRefinish
www.ppgrefinish.com.au
any refinish application. Backed by time-saving colour tools and support, the Deltron refinish system provides the confidence of working with a total solution that ensures you never lose your shine!
contents
3
OCTOBER 2018
SC A N TO RE A D T HE REFINISHER ONLINE
60 VOLUME
Vol 1 No1
1959
Vol 60 No1
2018
THE
REFINISHER
ISSUE 3
Editor-In-Chief Paul Galea
6
Editorial Co-ordinator Rachael Siotas
4
News
6
Top of the class
Editor John M Stanley Creative Director Dean Parrott
DELTRON® sets a new benchmark for solvent-borne performance
Published for and on behalf of PPG Industries Pty Limited by
Kisschasey Creative Pty Ltd Unit 113, 91 Murphy St. Richmond, Victoria, 3121 Telephone (03) 9421 3311
14
14
A new clearcoat which really shines
16 Australia Head Office Locked Bag 888, Clayton South, Victoria 3169. McNaughton Road, Clayton, Victoria, Australia, 3168 Telephone: 13 24 24 www.ppgrefinish.com.au New Zealand Head Office 5 Vestey Drive, Mt Wellington, Auckland, New Zealand. Toll Free Telephone: 0800 320 320
22
New South Wales 10 Peter Brock Drive, Eastern Creek, 2766 Telephone (02) 9854 6600
Western Australia Unit 2/6 Colin Jamieson Drive, Welshpool, 6106 Telephone (08) 9256 3920
PPG Logo, Delfleet, Deltron, Envirobase, Global Refinish System, Harlequin, PaintManager, Prizmatique, Radiance, RapidMatch, Startline and Vibrance Collection are registered trademarks and Bringing innovation to the surface, Crystallance and RapidMatch are trademarks of PPG Industries Ohio, Inc. SATA and SATAjet are registered trademarks of SATA GmbH & Co. KG. Third-party trademarks referenced in this magazine are the property of their respective owners.
Flow on effect Building on the CT Green Belt Training program
Queensland 18 Breene Place, Morningside, 4170 Telephone (07) 3823 8000
Tasmania PO Box 406, Kings Meadows, 7249 Telephone 0412 254 807
Re-mastered-piece With models like the Speedback GT and Mini Remastered, David Brown Automotive offers sexy ’60s style with a modern, high tech twist. For the retro-inspired colours to suit, the exclusive British brand went straight to PPG
16
Victoria 104-106 Woodlands Drive, Braeside, 3195 Telephone (03) 8586 0000
South Australia 1E Oldsmobile Terrace, Dudley Park, 5008 Telephone (08) 8346 6870
Sheen with EN-V
30
Sensors & sensorabilities Sensors are set to drive the autonomous future
32 32
Problem solvers MaxiTRANS has the solution
NEWS 4 REFINISHER
5
minutes of fame T
he arrival of PPG’s breakthrough LVC-105 EnviroFIVE™ Clearcoat has generated plenty of excitement in the market. It’s not just the amazing ability to cure in as little as five
minutes, it’s also the fact that it backs it up with easy application and a clear, clean, gloss finish straight off the gun. Now there is a fun video which helps to highlight these attributes. It features a hapless valet parking attendant who take advantage of
EnviroFIVE to fix an awkward situation. You can watch the short video by visiting www.ppgrefinish.com.au and clicking on the link, by going direct to the YouTube site https://youtu.be/Pq8tshe20UY or by using R the QR code on this page.
Commercial Performance Coatings on show at Land Forces D efence force applications are some of the most challenging coatings environments on earth but it’s where PPG’s Commercial Performance Coatings thrive. In early September, Adelaide played host to the Land Forces 2018 event which was all about showcasing equipment, technology and services for the armies of Australia and the Indo-Asia-Pacific region, and Commercial Performance Coatings was front and centre. The locally developed and manufactured range of APAS approved products is already used on a wide range of
Australian Defence Force projects, including for the Bushmaster and Hawkei vehicles which are being produced by Thales in Bendigo, Victoria. Via an onsite stand, attendees at Land Forces 2018 were able to
chat to PPG staff and learn more about how the specialised range of Commercial Performance Coatings products has been perfectly adapted to the needs of these R ADF projects.
Free online airbrush magazine
go to . . . www.airvolution.com.au
It’s all about the Australian and New Zealand airbrush community, people, events and competitions.
Airvolu tion •
The ma
gazine
for the
living
Issue
airbrus
h movem
• Stud ent inter views • ush Vent uri news • Meet •
• Airbr
• Quar
Mr Tony Vowles • Cert • II in Airbr ushin terly Airbr g• ush comp etition •
1 • June
ent
2010
NEWS 5 REFINISHER
DRIVETHROUGH
with Paul Galea
Getting set to
‘match it with the best’ T
he 2018 edition of the annual PPG Colour Matching Competition is building towards an exciting finale. After kicking off in June with the Northern Territory’s preliminary competition where Blair Keller took the win, a host of young spray painters across the region have taken up the challenge, won through and booked their place in this year’s ANZ final. As well as promoting colour theory and colour matching practical skills amongst apprentices across the region, diversity is also a winner thanks to Lucy Grimwood’s win in the South Australian competition.
Winners will gather for the 2018 final in Brisbane where they will ‘match it with the best’ to see who will be crowned PPG Colour Matching Competition champion. As well as the chance to take home the winner’s trophy, there are also great prizes on offer, including gift vouchers, SATA spray equipment and MIRKA tools. Keep an eye out for coverage of the PPG Colour Matching Competition final in the 4th issue of The Refinisher.
R
Sidchrome Project Car tools up for 2018 S
leek, menacing and beautifully finished in Nardo Grey PPG paintwork, the 2017 Sidchrome Project Car was a ’69 Mach 1 Mustang like no other – eventually being won by a lucky South Australian resident. Now the well-known and popular tool brand is at it again with the 2018 Sidchrome Project Car promising to take the build to the next level. This will be the project’s fourth consecutive
year – after a VW Combi in 2015, a Python Vehicles Cobra in 2016 and the Mustang in 2017 – and follows a similar formula where an iconic older vehicle will be pimped to the max, including a stunning paint colour courtesy of PPG. For a chance to win this incredible vehicle, check in at www.sidchrome.com.au or at your R Sidchrome stockist.
2018
I
hope you have been following our series of articles on attracting the next generation of apprentices to our industry. Suitable young people are out there and, in the latest instalment (pg 24), Gavin Cribb from Kangan Institute in Melbourne gives some great insights into how to not only attract them to your business but also how to keep them engaged and heading in the right direction. PPG continues to support training providers across the region to help ensure that the apprentices who are coming through the system get exposed to the latest in technology. If you do have the opportunity, I urge you to make apprentices part of your business. Speaking of technology, it just keeps on ramping up and the latest updates to our premium solvent-borne paint system are a great example. The DELTRON® refinish system has been a long time favourite right around the world and we have been able to draw on that global technology and then refine it in our local laboratories in Clayton. What it means is that local customers get the very best technology available in primers, basecoats and clearcoats, as well as hardeners and thinners. We are also bucking the trend by continuing to manufacture locally. Indeed, virtually all our refinish product lines, including the Deltron solvent-borne system and the LV range of ENVIROBASE High Performance products, are manufactured right here at our Clayton production facility in Melbourne. R Enjoy this issue of The Refinisher!
PRODUCT NEWS 6 REFINISHER
Top of the Featuring global technologies and local tuning, the popular
class
DELTRON® refinish system gets a fresh look while setting an all new benchmark for solvent-borne performance.
DELTRON® refinish system
O
ver the past couple of decades, the Deltron paint system has carved out a well-earnt reputation as a tried and proven solvent-borne solution that delivers outstanding real-world performance, from productivity and colour capability to user-friendliness and durability. And this scenario has been
repeated in markets all over the world, including locally where it has cemented its place as the region’s most popular solventborne refinish system. Having said this, the local development team did not see all the success as a reason why this long-term favourite could not be improved even further and the transition to new global Deltron paint system branding has provided the perfect opportunity. The comprehensive update process kicked off by gathering detailed customer feedback on existing products to find out what painters liked and where improvements could be made. Armed with this information, the R&D team within PPG’s Clayton headquarters began searching through the advanced product technologies available throughout PPG’s global network. In this way, they were able to take advantage of the latest coatings building blocks to create a selection of next-generation primers, clearcoats, thinners, hardeners and additives.
Locally tuned, locally manufactured Importantly for local users, the R&D team has formulated and tuned these new products to specifically meet their needs, in terms of both application, performance and long-term durability. For example, the clearcoats have been formulated with plenty of UV absorber to help them cope with the harsh local conditions which
PRODUCT NEWS 7 REFINISHER
Clear, logical branding While the fresh global branding does not play a hand in the system’s outstanding performance, it is a significant convenience feature for painter who are using these products every day. Indeed, a lot of thought has gone into ensuring it is as logical and clear as possible. To begin with, you will notice that each product type (clearcoat, primer, hardener, etc.) uses a different colour. The ‘DELTRON’ name features boldly on each label, as does the product code and product description. Each product code features two letters, followed immediately by three numbers. The first letter is ‘D’ for Deltron, while the second letter indicates the product type: can break down products that are not prepared for it. While it might be packed with global technology, the updated Deltron paint system is manufactured locally from high quality raw materials, just like the superseded range. Not only does it highlight PPG’s commitment to local manufacturing, it also gives greater responsiveness to the needs of regional customers.
What’s new? The first thing most people will notice is the fresh new branding for the entire Deltron paint system. New product technologies will arrive with the updated branding while the Deltron tinter range will changeover as existing stock runs out and is replaced by new stock. It is important to note that the tinters themselves will retain the current number system which people are familiar with and the tinter formulations and, hence, the contents of each tin remain the same. Before getting into the new primers and clearcoats, it is worth pointing out that the new thinners and hardeners are also a significant feature. Indeed, the majority of the thinners and hardeners (in a variety of different temperature ranges) are shared across nearly all of the primers and clearcoats. This is not only convenient, it also keeps the entire Deltron paint system very compact and reduces the amount of different stock holdings for customers. No less than seven new
primers will be available to choose from under the updated Deltron paint system. As well as giving repairers the ability to tackle any refinish situation with speed, efficiency and a solid foundation, they also come with the convenience of sharing thinners and hardeners across most of the range. Several also offer the option of using an accelerated mode when a job needs to be pushed through quickly. To literally provide the finishing touch, three new clearcoats arrive to give customers a wide choice of options to cover any type of application. For extra convenience, all three share the same thinners, and hardeners as well as the option of selecting an ‘accelerated mode’ by using a specific thinner. While a new look is the giveaway for the updated Deltron paint system, customers will quickly find that the compact system gives them everything they need to maximise performance, productivity, ease of use and dependability.
C = Clearcoat
T = Thinner
P = Primer
A = Additive
H = Hardener This logical labelling continues onto the hardener and thinner range where the last two digits of the product code signifies the temperature / speed at which that product is intended to be used:
10 – Fast (10°C to 20°C or spot repairs at 20°C to 30°C) 20 – Medium (20°C to 30°C or spot repairs at high temps) 30 – Slow (30°C to 40°C or large areas at 20°C to 30°C) 40 – Extra Slow (40°C and above) Note: These temperature ranges are for guidance only since other parameters, such as spray gun setup, humidity and speed of air movement, may require a different hardener / thinner combination for optimal paint application.
PRODUCT NEWS 8
Top of the class
REFINISHER
Primers
DP612 EtchPRIME
DP616 EpoxyTHANE
No matter what the job or the substrate, the Deltron paint system has an efficient, easy to use primer which can be used to lay down a solid foundation for the following layers. Features include, excellent Wet-On-Wet (WOW) options, accelerated options and spectral grey shades to help improve topcoat coverage.
This chromate-free primer has a virtually universal application as an adhesion promotor over a wide range of substrates – it is particularly recommended on bare metal substrates, including aluminium and galvanised steel. If required, it can be used in a WOW system when overcoated with most types of Deltron 2K Primers.
This epoxy urethane primer offers excellent adhesion to steel, aluminium and galvanized steel and should be used whenever optimum corrosion protection is required – bare metal surfaces, under polyester spray or hand applied body fillers and Deltron primers
DP618 PrimaBUILD
DP614 EpoxyPRIME
This versatile, high build 2K primer offers exceptional film build when used as a spray filler or primer surfacer. As well as sound, fully-cured original paintwork, it can be applied over suitably prepared polyester putties and it can be flexibilised for use over plastic parts.
Versatile and with good adhesion to a wide variety of suitably prepared substrates, EpoxyPRIME is ideally used as a WOW or non-sand surfacer, however it can be baked or air-dried if required. It can also be used as a one-coat sealer over flattened Deltron primers and surfacers, where it fills sanding marks and rub-throughs and promotes optimum gloss holdout in the topcoat.
DP602 PrimaPRIME Versatile, quick-drying and easy to apply and sand, this grey 2K primer-surfacer offers excellent corrosion resistance, film build, surface levelling and gloss holdout over a wide range of substrates which makes it ideal for a wide range of day-to-day repair work. By simple adjustment of the thinning ratio, PrimaPRIME can be applied as a conventional primer surfacer, a high-build spray filler or as a WOW surfacer and there is an accelerated mode which cuts the bake time to just 20 minutes.
DP620 PrimaSEAL When refinishing electrocoated panels, OE or other sound paintwork, the extraordinary adhesion promoting characteristics of PrimaSEAL make the job significantly quicker by eliminating the need for detail sanding of the substrate. It promotes excellent gloss holdout, can be used in high productivity WOW mode and, because it is transparent, PrimaSEAL is especially suited to respray work where it avoids the need for detailed masking around door-shuts, panel edges, etc.
“No matter what the job or the substrate, the Deltron paint system has an efficient, easy to use primer which can be used to lay down a solid foundation for the following layers.”
PrimaGUARD (DP621 PrimaGUARD G1, DP625 PrimaGUARD G5, DP627 PrimaGUARD G7) Formulated using the latest primer technology, this product is perfect for optimising the priming process. Available in three spectral grey shades, it not only delivers strong adhesion, it also features very smooth flow which means no sanding is required on new electrocoated panels. It can be topcoated immediately after flash-off or up to 24 hours later (at 20°C) with no sanding required – perfect for batch priming new panels!
PRODUCT NEWS 9 REFINISHER
DC516 GenCLEAR Easy to use and polish and with a glossy, durable final finish, this high performance acrylic urethane clearcoat is designed for everyday jobs from a single panel to a full respray. And, when a job needs to be processed quickly, there is an accelerated mode which cuts the bake time to as little as 20 minutes.
DC527 SprintCLEAR
Clearcoats As well as easy to recognise naming, all three of these next-gen clearcoats share thinners and hardeners and they have an accelerated mode using a specific thinner. Keep all three on the shelf or choose the one which suits you best – either way, you can’t lose!
DC501 OptiCLEAR As the name suggests, this is a premium
quality clearcoat specifically formulated to give optimum durability and glossy final finish. Versatile enough to be used on anything from a single panel to a full respray, it also features an accelerated mode which drops the bake time to as little as 20 minutes.
When there is the need for speed combined with a quality, high gloss final finish, this premium, High Solids polyurethane clearcoat has the answers. It starts with the ability to be used in high productivity single visit mode (a light closed coat, immediately followed by a full wet coat) or conventional two coat mode. Combine this with the accelerated 15 minute bake time and it is the perfect solution for a fast paced modern R collision centre.
PPG CUSTOMERS 10
BIGFOOT 4X4 INC.
REFINISHER
Bigger
T
he story of how one monster truck brand invented an entirely new category of spectator entertainment is, at its core, a family affair. Like many great inspirations, the creation of the BIGFOOT® Monster Truck Enterprise was the answer to a simple question: How can one resourceful dad better equip his 1974 Ford F-250 pickup to handle the rigors of his family’s off-roading, 4x4 weekend adventures? For Bob Chandler, from the US city of St. Louis in Missouri,
is better! The BIGFOOT® Monster Truck
Enterprise extends its brand image worldwide with a little help from PPG.
transforming his pickup into the world’s first monster truck was a natural evolution.
Small beginnings “In the early 1970s, BIGFOOT started out as a family vehicle. My father worked construction but also taught himself how to do things,” explains Ann (Chandler) Trent, Bob’s daughter and President of BIGFOOT 4x4 Inc. “It began with bigger tyres. As time went on, the truck kept growing. Bigger tyres led to military axles and bigger motors. On the weekends, we’d go four-wheeling and attend some tractor pulls.” Slowly but steadily, the BIGFOOT legend grew, leading to more appearances, bigger car crushes and a following of rabid fans. Soon Chandler and his signature
PPG CUSTOMERS 11
monster truck became well-known names across the Midwest, turning a family hobby into a viable business opportunity. “My dad borrowed money from one family member and rented a building from another to work on the truck and develop parts for the fourwheel-drive community,” recalls Ann. “By 1983, we had so many bookings that he and his partners made a second truck – BIGFOOT #2.” Fast forward to the mid-1990s and the BIGFOOT stable had grown to an astonishing nine vehicles. By this time, the Chandler’s shop had ceased doing their four-wheeldrive work and the focus was on building the BIGFOOT brand in the fast-growing segment of motorised entertainment.
Globally recognised brand Nowadays, while Chandler has passed day-to-day control of the BIGFOOT operation to Ann and her husband, Bob, his commitment to the company as the global leader in this unique performance segment has never wavered. “Our business is not like any other industry,” Ann explains. “We’re in the trucking business, we’re an entertainment property and we’re a promotional and licensing company. Even when the economy is bad, we do well because our ticket prices are a good value for families.” Now 40-plus years after its humble beginning, Ann points out that the
BIGFOOT brand still generates incredible enthusiasm among fans – as evidenced by its recent appearances at Major League Baseball’s All-Star Game Fan Fest, the NHL Winter Classic and events overseas. “We went to Kuwait and BIGFOOT performed car crushes for the U.S. troops stationed in that region. The reaction we received was incredible; they had the best time.” Today, the BIGFOOT team consists of 20 employees, five race trucks, three display trucks, drivers, mechanics and one very talented painter named Scott Upchurch. Most of the work takes place at a fullservice facility in Pacific, Missouri, which is equipped to address virtually any scenario imaginable.
The BIGFOOT – PPG partnership So how did one of the most successful automotive performance brands in the world end up partnering with a global leader in refinish technology? According to Bob Trent, the relationship started with typical networking at a trade show where he met Steve Lehner, PPG’s Product Manager for premium solvent brands.
“We had a great conversation and quickly realised our organizations shared similar values,” recalls Trent. “We’ve had relationships with other paint manufacturers in the past and, when we were looking for a new partner, we felt PPG stood out. Our trucks make 700 – 800 appearances a year, and we go through a ton of body parts. We take great care in how our trucks look.” Consequently, the BIGFOOT paint operation now relies on a suite of high performance PPG refinish products, as well as VIBRANCE COLLECTION® custom colours and finishes, to meet its expectations – with colour consistency among their key performance criteria. “BIGFOOT is racing all over the world, so it’s important that there is repeatability and consistency with our paint,’ says Don Peters, PPG Territory Manager. “The colours have to match and deliver good quality again and again and again.” According to Don, an important factor in bringing this point to fruition is the backing
PPG CUSTOMERS 12
BIGFOOT 4X4 INC.
Bigger is better!
REFINISHER
GOING BIG!
BIGFOOT receives from its PPG Platinum Distributor, Licari Auto Body Supply, that is responsible for colour mixing, product delivery and technical support. Scott Upchurch is the person most responsible for ensuring that paint finishes on BIGFOOT’s trucks meet the high standards for the brand’s image, with PPG’s help. “We sent PPG a hodgepodge of colours we used throughout the years, and they came up with custom baseline colours for our trucks.” Upchurch extolls the performance of PPG products. “We pressure wash these trucks over and over again and we have had zero issues. The clears dry super-fast, which is important because oftentimes we only have a one or two-day turnaround time. And a lot of basecoats don’t work well when you’re airbrushing effects, but PPG basecoat works great.”
While the partnership between BIGFOOT and PPG may be in its infancy, these two iconic brands in their respective arenas are continuing to work together to push the envelope of possibilities and the results speak for themselves. “Being at the show and sitting in the stands, looking down, you can tell the difference between our PPG-painted trucks and the others,” notes Upchurch. “It’s quite obvious.” With over four decades of history-making behind them, Team BIGFOOT is showing no signs of slowing down. As the monster truck industry continues to grow and evolve as a spectacular spectator experience, you can rest assured that Team BIGFOOT will continue to set a high standard of class, R performance, and innovation.
The list of accomplishments compiled by the BIGFOOT team over more than four decades is quite remarkable. To date, Team BIGFOOT has amassed a remarkable 48 championships! What’s more, BIGFOOT #5, #14 and #18 have all held or currently hold Guinness World Records, the most recent of which was #18’s incredible long jump of 214 feet 8 inches (over 65.4 metres). Thanks to its enduring popularity, BIGFOOT has visited more than 26 countries and has appeared in literally hundreds of TV shows, from televised races to cartoons to documentaries. It has also been a big hit in Hollywood movies, with the latest being in Steven Spielberg’s ‘Ready Player One’. This includes an extensive BIGFOOT #8 cameo during most of the big VR race scene at the beginning of the movie. The truck is driven by one of the major characters’ avatar, and shares much of its time on screen with the ‘Back to the Future’ DeLorean driven by the movie’s star. Children’s toys is another area where the team has had a big impact – over four million BIGFOOT toys have been sold worldwide since 2014. Adding to the team’s accomplishments was the late 2009 announcement that BIGFOOT had been named one of the Top 5 Marketing Vehicles of all time.
PPG IN ACTION 13 REFINISHER
Aussie Invaders
With the incredible ability to accelerate from 0 to 1,600kph in just over 20 seconds and a PPG paintjob to match, Aussie Invader 5R is getting set to write its name into history.
M
ore men have walked on the Moon than have driven a car at over 600mph on land, according to Rosco McGlashan. Born in Perth in 1950, Rosco has been hooked on coaxing speed out of wheeled machines ever since. In 1994, he broke Donald Campbell’s Australian Land Speed Record with a car, called Aussie Invader II, at 500mph (802kph) and then crashed it at nearly 600mph attempting to raise it further. At the wheel of a new car, Aussie Invader III, in 1996, Rosco recorded a one-way pass of 638mph (1,028kph). This was actually faster than the record at the time, however it had to be backed up with a second run in the opposite direction within one hour and this was prevented by bad weather. In the meantime, a British team raised the bar even further, breaking the sound barrier and hitting 763.035mph (1227.985kph) in 1997 and this record stands today. Despite being the fastest Aussie on earth, Rosco isn’t content and his determination to become the fastest man on earth has seen him gather an exceptionally talented team to build ‘Aussie Invader 5R’. Weighing in at 9.2 tonnes when loaded with fuel, this incredible machine is powered by a single rocket motor which produces 62,000lb of thrust (around 200,000 horsepower) and is capable of accelerating from 0 to 1000mph in just 20 seconds.
The project has already secured the backing of a strong supporter group, including PPG. As a result, the 16-metre-long car has been given a suitably stunning paintjob (using Deltron basecoat and Delfleet Evolution primers, clearcoat and direct gloss) which was applied by long-time
PPG customer, Parins Truck and Machinery Repair Specialists, in Perth. PPG’s WA State Manager Refinish, Brad Curtis, says it’s been great working with Rosco who was actually awarded the Order of Australia Medal (OAM) in 1998 for his services to motorsport and for setting a new Australian Land Speed Record. “Rosco McGlashan is a legend in the World Land Speed Record community and we are proud to be able to contribute to his latest effort. At its first public display in May, at the Motor Pavilion Perth, Aussie Invader 5R stole the show with thousands of people flocking to see this amazing machine up close. Rosco has huge drive and determination so I will not be surprised at all to see him go on and realise his dream!” R
To achieve the World Land Speed Record, the speed is measured over a one-mile course and is averaged over two runs in opposite directions which must be completed within one hour of each other.
PRODUCT LAUNCH 14 REFINISHER
EN-V
Sheen with Formulated using PPG’s advanced resin technology, the new LVC-136 EN-V™ Performance Clearcoat produces a luxurious gloss finish the envy of other clearcoats.
R
eproducing the ‘factory’ appearance of a vehicle following an accident is not just about colour. Naturally, the final clearcoat layer plays a key role and it is here that the new LVC-136 EN-V Performance Clearcoat provides a production-friendly solution for modern repairers. This next generation clearcoat arrives as part of the ENVIROBASE® High Performance paint system and is designed to deliver superb gloss, along with a host of other benefits.
Next gen technology To create EN-V Performance Clearcoat, PPG’s R&D team delved deep into the company’s technology toolkit. As a result, this all new clearcoat incorporates advanced resin technology which not only gives it easy mixing and application characteristics, with fabulous flow and levelling qualities, it also allows it to produce a crisp, clear factory appearance. While it can be relied on to deliver an excellent appearance straight off the gun, it’s also easy to polish, if required. As an added bonus, EN-V Performance Clearcoat shares its hardeners and thinners with the rest of PPG low-VOC clearcoat range which makes for simpler mixing and less chance of errors, as well as meaning that less stock needs to be held.
Versatility and speed As part of PPG’s complete low-VOC solution, EN-V Performance Clearcoat is a premium Ultra High Solids polyurethane
clearcoat which is primarily designed to be used over Envirobase High Performance basecoat. Thanks to this next generation formulation, it’s a clearcoat that is versatile enough to fill virtually any role from one panel to a full respray and still generate a premium gloss finish. When required, EN-V Performance Clearcoat can also meet the need for speed. Indeed, when using it in conjunction with the newly developed LVT444 Clearcoat Accelerator
Thinner, the bake time is slashed to just 15 minutes, thus giving the option to dramatically improve cycle-time on smaller jobs. Mixing is also very straightforward when used in accelerated mode – LVT-444 Clearcoat Accelerator Thinner is simply used at 100 percent. Combine a 15-minute bake time with single visit application mode (a light, closed coat over the whole job before immediately returning to the start and applying a full wet coat) and the benefits to productivity are significant.
PRODUCT LAUNCH 15 REFINISHER
Local manufactured EN-V Performance Clearcoat continues PPG’s long-standing commitment to utilising the latest in global coatings building blocks but to also manufacture locally. As a result, this new clearcoat, along with the majority of products in the Envirobase High Performance low-VOC range, are manufactured from high quality raw materials at PPG’s production plant in the Clayton suburb of Melbourne.
Part of the region’s most popular refinish system When the Envirobase High Performance waterborne basecoat system was integrated with a selection of next-generation primers and clearcoats featuring advanced low-VOC technology, it created a complete low-VOC solution for local repairers. It’s also a turn-key solution which is very easy to take advantage of without having to invest in expensive equipment. This unique blend of eco-friendly credentials and no-fuss ease of use, combined with outright speed and exceptional colour capability and accuracy, has seen repairers flock to the Envirobase High Performance paint system. As a result, Envirobase High Performance sets the benchmark as the region’s most popular refinish system – bar none!
The complete low-VOC solution
Features of LVC-136 EN-V Performance Clearcoat • Simple mixing • Easy application • Easy to polish, if required • Advanced clearcoat resin technology • Excellent flow and levelling straight off the gun • Crisp, clear, premium gloss matches ‘factory’ finish • Accelerated mode for when a smaller job needs to be pushed through quickly • Shares hardeners and thinners
Fast! – exceptional speed and productivity 3 drive reduced cycle-times and increased
profitability Market-leading colour capability and colour accuracy Easy to identify low-VOC system, complete with next-generation primers and clearcoats Easy to blend and excellent aluminium control As market forces drive a shift to low-VOC technology, this is the high productivity choice Aligns with the majority of OE paint finishes which now use waterborne technology Supported by a full range of high tech colour tools Extremely user-friendly low-VOC system Outstanding durability under local conditions The peace-of-mind of the R PPG Lifetime Warranty
3 3 3 3 3 3 3 3 3
FEATURE STORY 16 REFINISHER
Re-mastered-piece By combining ‘60s chic with modern technology, David Brown Automotive offers the best of both worlds, in a handcrafted package complete with retro-inspired PPG paint finishes.
T
he 1960s was a golden era of high fashion and style, particularly as the automotive industry threw off the shackles of World War II austerity and produced some of the most elegantly beautiful car designs of all time. However, half a century down the track, choosing to drive one of these vehicles on a regular basis means also having to deal with ‘60s era functionality and drivability, not to mention reliability and safety. It’s a lesson British businessman, David Brown, learned the hard way. He borrowed a friend’s classic car to compete in a rally in the South of France but, after several days of overheating, poor performance and no modern conveniences, it finally broke down. Completing the rally in a run-of-the-mill modern hatchback got David thinking about how great todays cars are. What’s more, it planted the seed for the concept of designing a car that featured the timeless elegance of the ‘60s but came complete with modern-day performance, convenience, safety and technology.
Out of this love of both classic and modern cars, David Brown Automotive was founded in March 2013 and 12 months later its first model, Speedback GT, was launched. Just like the classic coachbuilders of the early 20th Century, Speedback GT is hand fabricated on an existing platform (similar to the Jaguar XK-R convertible and current F-type) which was chosen for its size and thoroughly modern lightweight aluminium monocoque structure. The skilled craftspeople at David Brown Automotive invest around 8,000 man-hours into each Speedback GT. Of this, 3,200 man-hours alone go into hand-rolling and beating the aluminium body panels. In April 2017, David Brown Automotive once again showcased its coachbuilding magic when it debuted its long awaited second model, Mini Remastered. Based on a classic, pre-2000 Mini (included in the purchase price), it’s designed to be the ultimate modern / classic city car, says David Brown. “The car has been subtly transformed and updated to retain the original’s DNA yet includes key design details from Speedback GT, as you can see by the grille, taillights and interior styling, as well as providing modern comfort and luxury.
FEATURE STORY 17 REFINISHER
However, it’s been important to remain true to Alec Issigonis’ wonderful original concept yet bring it into the 21st Century in our own way. We’ve had an amazing response to the car from Speedback GT customers and David Brown Automotive fans and we believe this is a car that will appeal to men, women, the young and old.” Each Mini Remastered is built by hand from the ground up taking more than 1,000 man-hours. Brand new body panels are refined by the craftspeople at David Brown Automotive to create smooth and accurate surfaces with perfect shut lines. The exterior shape has been refined, visually softened and ‘cleaned’ by de-seaming the silhouette and welding in bespoke structural beams and additional support struts for added rigidity. To ensure passenger comfort in the cabin, there is also a laborious sound-proofing process. Beautifully designed around modern convenience and luxury, the hand trimmed interior is swathed in leather and comes with a host of the latest features, including an in-built infotainment and navigation system with Apple CarPlay and Android Auto connectivity, USB connectivity and charging, keyless push-button start and remote central locking. A full four-weeks is set aside for the paint process which gives every car a flawless finish. To make their Mini Remastered truly bespoke, customers are encouraged to personalise their car using different exterior finishes, a contrasting roof, full interior trim and wheels, as well as further options and accessories. There is even the option to develop your very own exterior paint colour. It was around the time Speedback GT made its spectacular debut that David Brown Automotive first approached PPG to get advice on paint colours and finishes to best showcase its classic design elements. With Mini Remastered set to arrive, the partnership really hit its stride, says Michelle Gay, Sales & Marketing Director at David Brown Automotive.“We recognise the excellent quality and paint development abilities of PPG and it was a real pleasure to work with them again on the creation of an
18
Re-mastered-piece
REFINISHER
entirely unique range of colours that fit perfectly the personality of the model.” Each car undergoes an extensive, hand-applied paint process over four weeks. When it came to developing a bespoke range of colours for both Mini Remastered and Speedback GT, David Brown Automotive put its trust in PPG, according to David Rossiter, PPG UK Senior Colour Lab Manager. “With each Mini Remastered costing in the region of GBP £100,000, it was important that the colours we created reflected the prestige and exclusivity of the David Brown Automotive brand. We invited the company’s design team to PPG’s colour laboratory in Stowmarket and collaborated closely with them throughout the colour styling process. Initial colour samples and special effects were presented on individual panels before being painted onto small car shaped models for modification and approval. H A N D C R A F T E D W I T H PA S S I O N
S
taying true to the company’s roots was crucial when selecting a location for a manufacturing facility, design studio and headquarters. This saw David Brown Automotive move into a purpose-built 18,000ft² facility at Silverstone which is not only the historic home of the British Grand Prix but also an epicentre for automotive specialists and suppliers. A team of around 20 highly skilled craftspeople carry out the unique coachbuilding production process, says Michelle Gay. “It's the staff who make any business. Part of the reason we relocated to Silverstone was the wealth of skills in the area thanks to its motorsport heritage. That, coupled with the fact that we have really exciting products to work on and a great working environment mean it's much easier for us to find craftsmen and women than most companies. We also take on people who have the right attitude and passion for what we are doing and who are willing to learn.” For more information go to: www.davidbrownautomotive.com
“For Mini Remastered, we developed 12 non-metallic and two metallic colour options that would be sympathetic to the car’s retro styling and also showcase its fantastic shapes and panel quality. Together with David Brown Automotive, we had great fun taking our inspiration from classic rock ‘n’ roll songs to create shades such as ‘A Whiter Shade of Pale’, ‘Wild Thing’ and ‘Good Vibrations’.” The exclusive colour selection has not gone unnoticed in the marketplace, says Michelle Gay. “Every time PPG impresses us with the colours and finishes they are able to create. We always receive a huge amount of praise from both our customers and other companies within the industry on our paint colours and the Mini Remastered colour range has been no exception.” By drawing from the past while embracing the future, David Brown Automotive has carved out a reputation for style, craftsmanship and exclusivity. “We have a really exciting future ahead of us. We are increasing production capacity for both model lines in order to be able to reduce build slot wait times, which are currently over a year for each model. And of course, there are new projects on the horizon but these will remain in their infancy for some time whilst we fulfil the demand on Speedback GT and Mini R Remastered models.”
SATA 19 REFINISHER
Exclusive performance Two new special edition offers from SATA let spray painters take advantage of a little stylish individuality to go with the brand’s elite operation and functionality.
Celebrate as SATA turns 111 years old It’s remarkable to consider that SATA has been going strong for 111 years and as part of the company’s celebrations of this milestone it’s offering a limited edition ‘SATA Anniversary Bundle’. It features two high performance SATAjet 5000 B non-digital model spray guns which come with a laser engraved SATA Anniversary logo on the satin-chrome pearlchrome™ surface finish. Not only that, you also get a practical and stylish gun case to safely store the guns and avoid knocks and bumps when transporting them. Precision foam cut outs house the guns snuggly and there are extra spaces to store two SATA adam 2 digital air micrometers. Options include the ability to choose the two guns in RP technology or one in RP technology and the other in HVLP technology. It’s also possible to select from the most popular nozzle set combinations
used for basecoat and clearcoat application. Given this is a time limited special edition it’s best to get your order in now at your participating SATA distributor.
Direct from the USA Up until now, this special edition spray gun has only been available in the good old US of A but, since PPG is the SATA importer for Australia and New Zealand, the local team has managed to secure a very limited number for the ANZ market. The SATA PPGjet 5000 B comes with colourful and stylish graphics over the guns high quality, satin-chrome pearlchrome™ surface finish, featuring the traditional red, white and blue colours of the Star-Spangled Banner, along with a PPG logo. Like all SATAjet 5000 B’s, this gun is packed with features including outstanding versatility in terms of inlet pressure and application distance, as well as adaptability to the specific requirements of different paint systems. To avoid disappointment, get your order in now at your participating SATA R distributor.
TALKING TRAINING 20 REFINISHER
A cupboard full W of $avings By providing a means of utilising leftover topcoat material, the ‘Monday to Friday cupboard’ is a simple solution for minimising waste and putting dollars back in your pocket.
hat do you do with the topcoat material left over after a refinish job is done? If you are using PPG’s ENVIROBASE® High Performance waterborne basecoat system, which has a 90-day pot life, there is still a lot of potential in those leftovers. Perhaps, like many paint shops, you leave partially filled contains cluttering the mixing bench until they are eventually thrown out. This is waste, it costs the business money and there is a better solution, says John Hristias, PPG Business Support Manager Asia / Pacific, which is called the ‘Monday to Friday cupboard’.
How does it work? In an ideal world, a painter would mix the exact amount of topcoat to get coverage on the job and no more. However, in practice this isn’t an easy thing to do so painters tend to mix a little extra so they don’t run out. Given that some topcoat is left over after each job, the Monday to Friday cupboard provides an effective solution for making use of it. It is literally a cupboard with several shelves clearly marked with days of the week. The cost for a new cupboard is around $150 to $300 or you could re-purpose an old cupboard.
TALKING TRAINING 21 REFINISHER
SATA RPS Cups – the ideal storage container
Monday to Friday Remaining colour is labelled and stored in the Monday to Friday cupboard on the shelf corresponding to the day of the week on which the job was done. As a result, it offers a number of paint shop savings. Each colour is kept for a week so it can be used for touch-ups on the vehicle it was originally used on. For example, occasionally a job will come back to the paint shop because it needs a brush touch, a ‘blow in’ or a rectification. Because you know which day of the week it was done, it is a simple matter to go to the appropriate shelf, locate the labelled paint from the actual job and make use of it. This is a great time and material saving!
MONDAY TO FRIDAY CUPBOARD
Envirobase High Performance waterborne basecoat system has a 90-day pot life when stored in a sealed container and SATA’s RPS Cups provide a quick and highly effective solution. You can mix the paint in the RPS Cup, attach it directly to the spray gun and apply it to the job. Once finished, it can simply be removed from the gun, sealed, labelled and stored. One tip is to store the RPS Cups upside down so that the strainer in the lid stays wet. The alternative is to replace the filter and lid with a new one before using it on a job.
Simple low cost equipment example
• Cost – $150-$300 • ARC 2K - 6% Paint – $120 p/job • Reward? 100mL = $10 3 3 15 cars p/wk x $10 = $150 p/wk 3 $150 x 4wks = $600 p/mth
3 $7,200 p/a 3 8.3% of total paint spend ($86,400 Total Spend)
WHO’S GOT ONE? Do the sums
Rationalising Once the paint has been stored in the cupboard for a week it is unlikely to be needed for the original job but it isn’t thrown out – it can save money on future jobs! At certain times during the week, the stored containers in the Monday to Friday cupboard are rationalised. This involves taking any leftovers and combining them into their colour groups, i.e. all the silvers in one container, blacks in another, blues in another, etc. Empty two litre Envirobase bottles make handy containers and these colour group containers are then stored on another shelf where they can be used as a groundcoat on future jobs.
Material saving groundcoat Colour group containers can be kept for the term of their pot life but they are likely to be used well before then because they are perfect for laying down a groundcoat for similar colours. For example, on a silver job, simply take the ‘silver’ container from the Monday to Friday cupboard and use it to apply a groundcoat layer. It doesn’t matter if the colour is a little lighter or darker – I can tell you it works (in a similar way to a spectral grey groundcoat) and it won’t show through. It actually gives a double saving – using paint which was going to be thrown out means less of the actual vehicle colour is required to achieve coverage!
Look at the calculation below and, although the savings per job may not be huge, over time it can really add up to a significant amount. We have chosen conservative dollar figures and based the example on a small shop doing just three jobs per day. If you are doing more, you should save more. What’s more, this only takes into account the leftover product going into the Monday to Friday cupboard. Indeed, the saving is compounded so, if 500ml is used as a groundcoat on a job, it can actually save mixing as much as 500ml of fresh material. It is about making the most of the paint material which you pay good money for, getting rid of waste and using it to make a positive difference to your costs. Notes: ARC – Average Repair Cost Picked a figure of $2000 but could be more or less Average paint cost is around 6% per job which on $2000 ARC – $120 For more information speak to your PPG Territory Manager or MVP Business R Solutions Manager
MVP BUSINESS SOLUTIONS 22
COMMERCIAL TRANSPORT
GREEN BELT TRAINING PROGRAM
REFINISHER
Flow on effect After the spectacular success of the specialised CT Green Belt Training program, the initiative is set to have a positive impact on CT repairers long into the future. for Mike Gunnells – one of the highly
U
nlike their colleagues in light vehicle collision repairs, the Commercial Transport (CT) repair sector has not had to deal with significant pressures to lower costs and improve efficiency and productivity... yet! According to Greg Tunks, PPG MVP Business Solutions Manager ANZ, there is no reason to believe that a similar scenario will not impact CT repairers at some time in the future. “Even if you don’t believe that pressure will come from work providers, it makes sense to make changes and improvements to your business on your own terms. This was the key driver behind our initiative to bring the CT Green Belt Training program here in March and feedback shows it was extremely well received by the 50 people who attended. We arranged
experienced members of the US MVP Business Solutions team – to fly in specially to present the course.” Over a very busy three days, conference content was delivered in an easy to understand format while covering a variety of thought provoking topics, including strategic thinking, measuring and reducing repair cycle-time, lean methodologies, implementing change and much, much more. The key, says Greg, was to ensure that attendees left with a range of effective tools which they could use in their own workplace to achieve maximum results. “Repairers couldn’t get enough! The very day after the conference we got the first calls from CT businesses who wanted to follow up and keep pushing for constant
improvements. Given that our local MVP Business Solutions team also attended the CT Green Belt Training, they have been able to sharpen their own skills even further and are in a great position to support CT repairers across the region. CT repairers just need to contact us to start the process.” While there are obvious differences between light vehicle repairs and CT repairs, many principles for improving repair productivity and profitability are similar or even the same but on a larger scale. Greg says that a number of strategies which have already made a big impact in light vehicle repairs can be just as effect for CT. “The principles of 5S and waste management are exactly the same
MVP BUSINESS SOLUTIONS 23 REFINISHER
for light vehicle and CT repairs – it’s about increasing production. For example, 5S is about having an organised workplace where everything is in its place and easy to find when needed. When we talk about waste management, we are not talking about the rubbish the business throws out – it’s about waste in terms of time and motion. Everything is interconnected and when you have something that is not adding value to the business, you have waste which is a killer of efficiency and productivity.” “The way parts are processed is typically a huge issue – probably more so than with light vehicle repairs. CT repairers can benefit from X-Ray Repair Planning and meticulous disassembly but because the parts
are so bulky, they take up a lot of space which creates clutter. Having an organised parts department and dedicated parts area has been a big improvement for many car repairers and the benefits should be the same for CT repairs. Parts are ordered early, they come in and are allocated to the particular job. From there, they need to be removed from their box or crate and ‘mirror matched’ against the old parts to ensure they are correct and not damaged. Once this is done, the old parts should be disposed of to free up space and you can proceed with the job.” “Another current car repair concept that can transfer directly to CT is ‘doors open to doors open’ time. In this case, we are talking about making maximum utilisation of the spray booth but it applies just as much to any large piece of equipment. For example, the spray booth is designed for paint application,
flash-off and baking so the aim is to organise the production schedule so that other tasks are done outside the booth, thus ensuring it can be utilised to the full. The same can be said for equipment, such as floor racks and chassis aligners.” “In theory, the business of CT repairs should be no different to light vehicle repairs – just dealing with larger vehicles and parts. However, the MVP Business Solutions team recognises the subtle differences and, more importantly, the big opportunities for improvements. We have already seen business operators who attended the CT Green Belt Training go back to their shops and achieve very impressive outcomes. As a result, if we talk to a business owner and show that by implementing these proven strategies they can increase productivity by 10%, 20% or whatever it happens to be, we are confident it will happen. Irrespective of anything else happening in the market, that has to be a big incentive to start now.” R
APPRENTICES 24 REFINISHER
Next gen
attraction
Understanding the differences in the current generation of apprentices is a key step in attracting them to your business and retaining them long-term.
I
t may surprise people to learn that the average age for apprentices is currently estimated at around 22-years-old. Often, it means they have already had fulltime employment so they are more savvy about working rights, etc. This generation has also grown up having access to all the information they need on their phone so do not necessarily see the need to store it in their head. In addition, they do not appear to have job loyalty, but should they? The balance has shifted, says Gavin Cribb, National Training Manager at Kangan Institute in Melbourne, and it’s very much up to employers to create a work environment which engages and supports apprentices.
ATTRACTING STAFF
PART TWO
Advertising medium You often hear about businesses getting no replies to apprentice advertisements. However, where are they advertising? No prospective apprentice reads newspapers so it’s a waste of time, if that is your only
strategy. Social media is good but there are other more targeted options. Working with local schools can get good results and your training provider is often also willing to offer support. I know of several shops who do open days in conjunction with schools and it makes sense – it gives a chance to show off the shop. In addition, there are resources, such as ‘Jobactives’ and the Australian Apprenticeship Support Network (AASN) – both are Australian government initiative aimed at linking job seekers with employers. It’s also worth considering mature age apprentices – they can be an attractive option because they tend to be more stable and focused from the beginning and they potentially attract additional incentives for the employer. When advertising, it’s worth considering parents because they are often the ‘decision maker’. Look at your advertisement and ask, am I advertising a ‘job’ or a ‘career pathway’? Better still, ask someone else for feedback – you might be surprised!
Geography It’s not often considered but geography is crucial. It’s highly unlikely you will keep an apprentice who has to catch two buses or a connecting train – travelling to work becomes a chore. Consider where a prospective apprentice lives because you are much more likely to keep them if their work journey is easier.
Engage and understand It’s a sad fact that the average retention rate for apprentices across all trades is around 50%. There is a raft of reasons why but, to be on the positive side of this statistic, you must commit to apprentices and invest in their progress from the start. In the old days, it was seen as doing apprentices a favour by employing them and, therefore, they should be loyal to the business but it’s now the other way around. Employing apprentices is about ending up with a skilled tradesperson who will make money for your business. However, from the apprentice’s point of view – why make money for you if you do not treat them well when they can make money for another collision centre who looks after them better.
APPRENTICES 25 REFINISHER
Employers are often frustrated with the current generation. While there is typically a generation gap between owner and apprentice, one way to start engaging is to simply ‘listen’. It’s a bit obvious but we tend to tell them how things should be rather than getting their view of their training and work environment. Just taking the time to talk can give you a better understanding of who they are. Do you know what subjects your apprentice is studying next block? Anecdotal evidence suggests employers that do, have a much better success rate. If your apprentice’s upcoming block includes, say, ‘Paint Prep 101’, make sure you provide some work in this area BEFORE they go to TAFE. When they return, give them more work in this area – repetition equals knowledge retention. It’s also important to get apprentices doing ‘real’ tasks as early as possible. Rather than boring, menial tasks, giving
Training providers
them an opportunity to actually use a spray gun (this is the painter’s primary role!) can be invaluable for getting them excited about their career. They will make mistakes and it can be difficult for a busy shop but painting some old panels using leftover paint can be a cheap, easy way to keep their juices flowing.
It’s well worth collision centre operators having a conversation with their local training providers. Although there have been cutbacks to the funding of training providers, the TAFE system and the Australian government have worked hard to maintain a high standard of training. It has made for a very lean TAFE system but, in many cases, you will find world leading infrastructure, such as the Automotive Centre of Excellence (ACE) in Melbourne’s Docklands area, and there are others around the region. In general, training providers also offer far more flexibility in terms of scheduling when your apprentices attend. No one is saying that the system is perfect but, by working together, industry and training providers can continue to develop better solutions to attract R and retain apprentices.
PPG PEOPLE 26 REFINISHER
PPG Staff Profile
TonyThorpe O
ne key factor Tony learnt early in his career is that, on the whole, people choose to buy from people. In basic terms that means when it comes to the sales process, relationships and trust matter and it’s something which has helped him successfully tackle a variety of high profile roles at PPG. Having joined the industry as a 15 year-old panel beating apprentice, Tony honed his skills and went on to manage a couple of collision repair facilities before coming to the attention of the local PPG team.
Favourite hobbies /pastimes? Being a father and grandfather, sports with my children, diving and fishing Favourite food? Thai Favourite drink? Appleton Estate Rum Favourite music / band? Guns N' Roses Favourite car / motorcycle? AMC Javelin Favourite holiday destination? Rarotonga
Regional Sales Manager – NZ
“I think they recruited me for my relationship building skills – I joined PPG as Commercial Transport Manager for New Zealand and that sector is all about relationships. Over eight years, I found the role was a lot of fun while operating in a very professional manner, at the same time.” “Four years ago I moved to my current role where I basically looked after the top half of the North Island – I was excited and I saw it as a great challenge. We have a lot of quality repairers and distributors in a very busy market and I spend a lot of time with them keeping those relationships strong – it’s all about continuous communication. It’s also about having the right people around you and then nurturing and supporting them as they grow their skills and experience. At the same time, it’s great to see our customers grow their businesses and achieve their goals. Perhaps the most enjoyable part is seeing people succeed, whether it is customers or PPG staff – you can always learn from them as they overcome challenges in our R ever changing industry.”
MOTOR SPORT 28 REFINISHER
The process of winning What do top level Supercars racing and high productivity collision repairs share in common? Perhaps, more than you might think!
S
can the qualifying times at a typical Supercars event and you will often find the entire 26 car grid separated by less than a second. In one of the most competitive motor sport series on the planet, fractions of a second literally count! According to Ryan Story, Managing Director for DJR Team Penske, a long list of controlled components and tight cost constraints not
only fuel the close racing, they also attract highly competitive and highly skilled people to the category. A workforce of 42 personnel at DJR Team Penske are dedicated to one cause – winning! Despite all this, DJR Team Penske is still a business, with more similarities to collision repairs than may immediately be obvious. While the team’s ‘product’ is what it achieves on the track, how it goes about doing that, can be directly
related to a high productivity collision repair environment, Ryan explains. “Being successful in this business is about investment, processes and discipline. It’s about taking the time to critically assess our performance and where we can improve, making the investment accordingly – not just financial but also investment in time and people – and having the right discipline and culture to carry it through. This has been a key part of our journey to where we are now towards the front of the grid.” In a sport where tiny errors can have dramatic consequences, it’s processes which help to keep everything literally on track. This means step-by-step process covering every operation, just like PPG’s MVP Business Solutions team recommends for a modern collision repair workshop. “A structure of processes not only ensures that success is repeatable, it also means that if we do make a mistake, we can go back and determine what caused it and make a correction so it doesn’t happen again. You also need to evolve – you can’t simply continue to do what you have always done. For example, at the start of the 2018 season we found that we weren’t as competitive as we had been at the end of 2017. It doesn’t necessarily equate that what worked before will work
MOTOR SPORT 29 REFINISHER
again – we had to adapt and adapt quickly! We not only doubled down on our work and our time here in the shop but also in understanding what we could do to improve. We don’t necessarily have the fastest car this season but we have been making the fewest mistakes and, as a consequence, Scott McLaughlin is leading the championship.” According to Ryan, the influence of Roger Penske has further enriched the original team foundation set down by Dick Johnson. “Roger has been racing for 52 years and in business for even longer. You don’t have to look far to see why he has been so successful and how we can best structure ourselves to emulate that culture and level of success. It’s all about attitude and processes which we call ‘The Penske Way’. A big part is applying the principle of WWRD – What Would Roger Do? The Penske Way is striving to be your best – ensuring you represent the brand, the business and the culture in the best way possible.” Naturally, skilled people are crucial to the team’s success. With a limited number available with Supercars experience, DJR
Team Penske puts an emphasis on nurturing current staff and breeding new personnel. “When you have good people, you reward them and this is part of The Penske Way. We need to engage them and give them career pathways. As managers, it’s our responsibility to understand the aspirations and motivations of our staff. From my first days with the team, observing how Dick (Johnson) interacts with his people has been incredibly impressive. It’s the same today – when Dick comes into the office the first thing he does is go around and say hello to everyone and have a chat. Through that process you learn a lot about what is going on with each staff member. When you support your staff, you get the best out of them. It isn’t always easy and it doesn’t always suit the needs of the business but you have to have that long term thinking in mind.”
Despite the heartbreak of Scott McLaughlin being pipped for the Supercars Driver’s Championship, 2017 was a success as DJR Team Penske took the Team’s Championship, as well as Best Presented Team. “PPG paint is used on the chassis and every panel of our cars and finished with a mix of vinyl wrap and paint. Last year it made a strong contribution to our Best Presented Team award and it’s something we take incredible pride in. PPG has been a fantastic long-standing partner of Dick Johnson Racing from the early days and with Team Penske for over 30 years. As well as paints, we learn a lot from our interaction with PPG people and we look forward to sustaining that relationship long R into the future.”
AUTONOMOUS VEHICLES 30 REFINISHER
& sensorabilities
Sensors Just as humans rely on their sensors to navigate the world, so autonomous vehicles will need a suite of precision sensors to safely travel through and react to the surroundings.
I
magine being blindfolded and having to make your way through an unfamiliar building. Progress would involve potentially painful trial and error as you slowly felt your way forward. Autonomous vehicles cannot afford this approach. Instead, they will utilise a variety of sensor technologies to quickly and accurately map the fine details of the 360° environment around them and use this continuous stream of data to make decisions that will keep the vehicle on the road, follow road laws and avoid collisions with other road users (autonomous or not) and infrastructure. To enable level 3, or greater, autonomous driving requires a combination of three main sensor technologies – Radar, Cameras and LiDAR – which may also be supplemented by others, such ultrasonics and GPS. They can be fitted on the front, back and sides of a vehicle and each has its strengths and weaknesses.
Radar Perhaps the longest serving autonomous sensor technology, Radar actually stands for ‘Radio Detection and Ranging’. As the name suggests, it emits radio waves which bounce back from objects and are collected by a receiver.
This allows the system to calculate the distance objects are from the vehicle, the speed they are travelling and the angle they are facing. Typically, radar plays a key role in two lower level driver assist systems which have become very much mainstream – Autonomous Emergency Braking (AEB) and Adaptive Cruise Control (ACC). In contrast to LiDAR and camera technologies, radar is generally unaffected by environmental conditions such as darkness, bright sunlight, fog or rain.
Camera Given how sophisticated modern cameras are and the fact they offer an ‘eye-like’ view of the world, they would seem to be the perfect tool for autonomous driving. However, while they seem certain to play their part, using cameras alone presents issues. For example, lenses need to be kept clean and the image input tends to be affected by atmospheric conditions, such as bright light, shadows, darkness, rain and fog. Also, if multiple cameras are used to ‘stich’ together a bigger picture, each camera must be accurately and securely mounted to last the life of the vehicle and they require high graphic processing power in order to evaluate the inputs.
Camera LIDAR
Adaptive Cruise Control
Ultra Sound
They are relatively inexpensive and can fairly easily be packaged into modern vehicle design so many fledgling autonomous driver assist systems already use them for tasks including identifying lane markings and other common road network elements, such as speed signs, pedestrians, cyclists and vehicles. Cameras can be used in mono 2-D format or stereo 3-D format where two cameras are mounted a little apart from each other (much like our eyes) which helps provide depth perception.
LiDAR Short for ‘Light Direction And Ranging’, the basic workings of a LiDAR will be familiar to anyone who has used a DIY laser distance measuring tool. In basic terms, very short, high-power pulses of laser light are transmitted outward where they bounce off objects and are picked up by a highly sensitive receiver. Although LiDARs are not new, the technology is relatively new to the automotive sector and a lot of work is going on to refine and develop it and to seamlessly package it into modern vehicle architecture at a cost-effective price. Once fully developed, LiDAR technology has enormous potential for autonomous driving. It’s capable of scanning in all directions, out to around 300 metres, and generating an intricate map of the vehicle’s surroundings. By swiftly and accurately identifying the locations of stationary objects, as well
Long Range Radar
Lane Departure Warning
Emergency Braking Pedestrian Detection Collision Avoidance Traffic Sign Recognition
Cross Traffic Alert
AUTONOMOUS VEHICLES 31 REFINISHER
as moving objects, including their speed and direction of travel, it provides the sort of information required to react to varying circumstances on the road.
Smart paints to help cars ‘see’ It’s not only cars which are changing to support an autonomous future, the paints used to coat them and the surrounding infrastructure need to follow suit. PPG’s global R&D network is currently working on creating paints which not only look great but are also jampacked with functionality like never before. Collaborating with autonomous vehicle manufacturers will be a key factor in developing specialised coatings for infrastructure which will give vehicles the best means of clearly identifying their surrounds and communicating with other vehicles. Many people would be surprised at how much science goes into developing advanced coatings technologies. Today, darker vehicle colours absorb more infrared light which means that autonomous vehicle sensors have difficulty ‘seeing’ them. However, improved pigments and resins will absorb less infrared light and allow LiDAR sensors to see other cars better, no matter what the colour. In addition, hydrophilic and hydrophobic coatings
on the sensor covers and camera lenses will prevent the build up of dirt and enhance the sensors performance. Thanks to its strong OEM partnerships and credibility as a leader in the new
vehicle and refinish sectors, PPG is already well on the path to supporting an R autonomous future.
Wireless Communication
Surround View Park Assistance Surround View
Rear Collision Warning
Blind Spot Detection Park Assist Surround View
Short Range Radar
CT PARTNERSHIPS 32 REFINISHER
Problem solvers Problems are simply opportunities at MaxiTRANS, as the leading trailer builder creates and builds individual solution for customers, completes with PPG paintwork.
E
ach month the vast Ballarat production facility of MaxiTRANS Australia consumes a staggering 500 tonnes of steel, 300 tonnes of aluminium, 2376 tyres and 4.2km of air brakes hose, along with 175,000 line items. From these raw materials, a team of more than 500 staff build around 12 trailers a day and every one of them is custom made, according to Greg Brown, Technical Manager. “We see ourselves as problem solvers. Clients come to us looking for a trailer to perform a particular role. From there, the MaxiTRANS team work with them to determine exactly what their needs are and then our engineering department puts together the best package of features. In other words, we create the solution. As a result, you won’t find two trailers the same out there on the production floor.
We are custom builders and we have millions of different models. It gets mindboggling – as an extreme example, the trailer dimensions can vary in one millimetre increments!” There is a wealth of experience under the MaxiTRANS brand, along with a host of well-known trailer names, including Freighter, MaxiCUBE, Lusty EMS, Hamelex White, PEKI and AZMEB. Indeed, the organisation can trace its origins right back to 1946 when Freighter Industries was established. In 1998, MaxiCUBE made the logical move to purchase Freighter to create MaxiTRANS – where MaxiCUBE tended to specialise in van-type trailers, the Freighter brand complemented this with its well-known curtain-siders, flat tops and skels. This broadened the company’s market spread and was taken even further with a number of later strategic acquisitions which added tippers, bulk transfer systems and rigid truck bodies. Today, MaxiTRANS operates five production facilities – Ballarat, Brisbane, Melbourne, Auckland and China – and directly employs more than 1,000 people. At 30,000m², the Ballarat facility is the company’s largest and keeping the ‘custom’ production process running smoothly takes communication down to the finest detail, Greg explains.
CT PARTNERSHIPS 33 REFINISHER
“The difficulty in producing a customised trailer is getting each part in exactly the right place and it’s here that information is the key. Once the customer is happy with their trailer design, our engineering department creates a detailed set of drawings and a 3-D CAD model with all the parts. When that goes to the factory, it triggers the fabrication of some components and the ordering in of others and they come together on the production line. From there, the production team follows a set of processes and procedures that make it happen – everyone knows their part in the process.” Once components have been cut to exact size by the computerised laser or plasma cutters, they move to one of five production lines for welding and assembly. At the initial stages, special rotisserie devices allow the trailer to be rotated 360° to give staff members the most convenient angle to work from. After six steps along the production line, the partially completed trailer arrives at the start of the paint process where it continues its journey on an automated monorail system. It first passes through a
grit blasting booth before continuing on through three vast spray booths – the first for primer, the second for primer / topcoat and the third for final finish. Following the paint process, another nine stations take care of final assembly, although some are skipped depending on the type of trailer being built. From start to finish, it takes about one and a half to two weeks before the finished product rolls out the door. While sticking to set processes helps the production team deal with each custom build, an internal MaxiTRANS initiative means the aim is always to improve in terms of productivity, quality and safety, says Greg. “Between management and the shop floor staff, we are always looking at ways to do things better. Every day we are doing something – sometimes it’s a big refinement and sometimes smaller.
It might be about making an adjustment to the way we do things or it could be purchasing a new piece of equipment – MaxiTRANS isn’t backward in investing. Quality control is also extremely important. There is a long list of inspections made before each job is allowed to pass through a quality gateway.” Because all of the five production lines effectively funnel into the one channel in order to pass through the paint booths, this makes the speed, as well as quality, of the paint process key factors.
CT PARTNERSHIPS 34
Problem solvers
REFINISHER
Indeed, the ability to access high productivity solutions saw MaxiTRANS make the switch to PPG in mid-2016. Combining PPG’s DELFLEET® Evolution paint system, which was developed specifically for CT applications, with the market-leading technology of PPG’s F4949 CT Productive Chassis Primer Binder produced a result that was simply too good to ignore, says David Barendsen, PPG’s onsite Account Manager at MaxiTRANS. “When PPG introduced F4949 CT Productive Chassis Primer Binder, it created a totally unique solution to priming blasted metal surfaces, such as in trailer building, etc. Instead of having to choose between a 1K or 2K primer or an epoxy primer, customers can get the best of both worlds in one product. For MaxiTRANS, PPG was able to offer a significant improvement in productivity, headlined by a Wet-On-Wet process and a 33% reduction in bake time from 30 minutes to 20 minutes. This not only saves energy and reduces the company’s carbon footprint, it also improves cycle-time so more units can be processed in a given time.”
Given the improvements on offer, the switch to PPG made sense, according to Greg Brown, “MaxiTRANS does not make these changes lightly, particularly where we had the same paint supplier for around 12 years. It’s a commercial decision where the product has to work, the backup support needs to be strong and it needs to be at the right price. PPG give us that whole package, as well as having Dave (Barendsen) here to support us and, indeed, the entire resources of PPG. They gave us the opportunity to go from a 30-minute bake cycle to 20 minutes. That is a 33% saving, straight up, and on top of that we take advantage of the ability to sympathetically colour the F4949 primer. Putting coloured primer underneath the topcoat not only means that we get coverage more quickly, it also means that any scratches or stone chips won’t stand out.” “Colour is another important factor, even on a trailer. To match their fleet livery or just their preference, customers will specify a new colour every day and, in this industry, you have to be able to supply whatever they want. We offer tens of thousands of colours – it doesn’t matter what it is, PPG will match it and mix it for us. The finish just keeps ramping up because customers expect it to. For some, their rig is their pride and joy – it’s like buying a new car and they want it to look like that. The paint finish is the thing you see first and it has to keep getting better and PPG is there to support us in doing that.” By providing a package of high tech products and close support services PPG has solved a problem for MaxiTRANS in the same way the leading trailer manufacturer solves problems for its many customers! R
ENGINEERED FOR EXCELLENCE
Thanks to an unrivalled combination of exceptional speed, superb colour accuracy, no-fuss ease of use and effortless blending and mottle control, this is simply the best refinish technology on the market. Backed by a range of primers and clearcoats featuring advanced low-VOC technology, it’s the eco-friendly choice which really delivers on outright speed. With everything a 13 24 24
modern, fast-paced collision centre needs to slash cycle-time while
@PPGANZRefinish
www.ppgrefinish.com.au
boosting productivity and profitability, EnvirobaseÂŽ High Performance is engineered for excellence!