2022
BMHR A SUPPLEMENT TO WORLD CEMENT
THE NEXT GENERATION OF INDUSTRIAL BUCKETS
NylathaneTM Buckets
✓
NYLATHANETM
AC
Tough & Resilient Non-Corroding
Self-Cleaning, Anti-Stick Surface Up To 75% Lighter Than Steel
AA
ꭙ
STEEL
Deform Permanently With Impact Can Corrode Lose Capacity With Sticky Product Heavy
MF
READY TO SHIP! MORTON, IL USA
4B Components Ltd. • 309-698-5611 • www.go4b.com/usa
CONTENTS DOMES, SILOS, & STORAGE 04 Massive Storage Meets Sophistication Rebecca Long Pyper, Dome Technology, reports on a recent collaboration between Lehigh Cement Company and Dome Technology to build the world’s second-largest clinker storage. 10 Growing With The Region Daniele Sciuto, Euromecc s.r.l., describes the technical solutions adopted to upgrade SOCOCIM Industries’ Rufisque cement plant in the Dakar region. 15 Fixing The Mixing Wen Peng, Henan SRON Silo Engineering Co., reports on the installation of an advanced powder mixing system installed for a Korean cement company. SILO CLEAN-OUT & REPAIR 19 Getting The Most Out Of Your Silo Jeremy Snyder, Mole•Master, provides an inside look at the benefits of silo cleaning and maintenance for a cement processing facility. 23 Silo Repair In Spain Aquajet details a successful silo repair project for a cement plant in La Robla, Spain. 27 Keep It Moving! Primasonics describes the role of acoustic cleaners in preventing material build up and maintaining continuous flow in the cement silo. CONVEYING 30 Ahead Of The Curve Dr. Andreas Echelmeyer, BEUMER Group, outlines an innovative planning method for curved overland conveyors designed to provide customers with a high efficiency, long distance conveying solution.
CHAINS 47 Identifying The Weak Link John King Group reviews a case study detailing an elevator chain installation and the subsequent attempts to ensure optimal operation. BAGGING & PACKING 52 Efficiency Is Key: Transporting And Storing Alternative Fuels Aino Saarelainen and Panu Kantosalo, Cross Wrap Oy., discuss how increasing freight costs affect the use of alternative fuels in the cement industry and assess ways in which these costs can be best minimised. 59 Cutting Emissions: One Bag At A Time Sigrid Eder-Ince, Starlinger & Co., explains how optimising cement packaging will be a major factor in curbing the industry’s greenhouse gas emissions. ENVIRONMENTAL PROTECTION 64 Turning The Cement Industry Green Fabio Chignoli, Bedeschi, outlines the route that companies operating in the cement industry need to take to ensure the highest environmental standards. 67 A Decade Of Developments In Exhaust Gas Cleaning Georg Lechner, Head of Sales – Industrial Minerals at Scheuch, answers some questions to mark the 10th anniversary of the semi-dust SCR system and celebrate a decade of exhaust gas cleaning expertise. WORLD CEMENT Bulk Materials Handling Review 2022
36 Train To Maintain Jerad Heitzler and Todd Swinderman, Martin Engineering, talk about the importance of conveyor training as the key to successful bulk handling.
41 Conveying News Round-up World Cement presents a collection of recent news and technology updates from the conveying sector. Contributions come from: Brelko Conveyor Products, Doppelmayr Transport Technology, & ScrapeTec.
BMHR
2022
03 Foreword
A SUPPLEMENT TO WORLD CEMENT
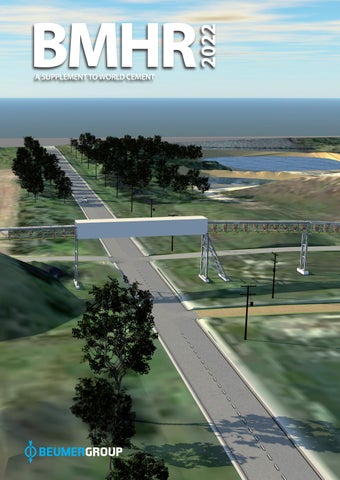
ON THE COVER Overland conveyors can move large quantities of material over long distances from the quarry to the plant. BEUMER Group relies on modern planning and layout tools to support operators at an early stage of the project and design the ideal conveying solution together with the customer. www.worldcement.com
For more information, read the article on pg 30 or visit: www.beumergroup.com
OFC_WCT_BMHR_2022.indd 1
2822_World Cement BMHR 2022_Titelseite.indd 1
24/08/2022 09:35
03.08.22 12:25
RopeCon® Efficient Solutions for Bulk Material Handling Wherever bulk material needs to go – across impassable terrain, rivers, highways and buildings – RopeCon® delivers without a hitch! Long distances, capacities of up to 25,000 tonnes/hour, minimal environmental footprint, quiet operation plus low operating and maintenance costs: These are the features that convinced leading mining businesses. doppelmayr-mts.com
FOREWORD Managing Editor: James Little james.little@palladianpublications.com
Senior Editor: Elizabeth Corner elizabeth.corner@palladianpublications.com
Editor: David Bizley
david.bizley@palladianpublications.com
Editorial Assistant: Sol Klappholz sol.klappholz@palladianpublications.com
Contributing Editor: Paul Maxwell-Cook Production
production@palladianpublications.com
Sales Director: Rod Hardy
rod.hardy@wpalladianpublications.com
Sales Manager: Ian Lewis ian.lewis@palladianpublications.com
Events Manager: Louise Cameron louise.cameron@palladianpublications.com
Digital Events Coordinator: Stirling Viljoen stirling.viljoen@palladianpublications.com
Digital Administrator: Leah Jones leah.jones@palladianpublications.com
Administration Manager: Laura White laura.white@palladianpublications.com
Reprints
reprints@worldcement.com
CBP006075
SUBSCRIPTIONS Annual subscription (published monthly): £160 UK includingpostage/£175 (e245) overseas (postage airmail)/US$280 U SA/Canada (postage airmail). Two year subscription (published monthly): £256 UK including postage/£280 (e392) overseas (postage airmail)/US$448 USA/Canada (postage airmail). Claims for non receipt of issues must be made within 4 months of publication of the issue or they will not be honoured without charge. Applicable only to USA and Canada: WORLD CEMENT (ISSN No: 0263-6050, USPS No: 020-996) is published monthly by Palladian Publications, GBR and is distributed in the USA by Asendia USA, 17B S Middlesex Ave, Monroe NJ 08831. Periodicals postage paid New Brunswick, NJ and additional mailing offices. POSTMASTER: send address changes to World Cement, 701C Ashland Ave, Folcroft PA 19032 Copyright © Palladian Publications Ltd 2022. All rights reserved. No part of this publication may be reproduced, stored in a retrieval system, or transmitted in any form or by any means, electronic, mechanical, photocopying, recording or otherwise, without the prior permission of the copyright owner. All views expressed in this journal are those of the respective contributors and are not necessarily the opinions of the publisher, neither do the publishers endorse any of the claims made in the articles or the advertisements. Uncaptioned images courtesy of Adobe Stock. Printed in the UK. Palladian Publications Ltd 15 South Street, Farnham, Surrey GU9 7QU, UK Tel +44 (0)1252 718999 Fax +44 (0)1252 718992 Email: mail@worldcement.com Website: www.worldcement.com
BMHR 2022 World Cement
DAVID BIZLEY, EDITOR
W
elcome to the 2022 edition of World Cement’s Bulk Materials Handling Review supplement, or BMHR. This special issue of World Cement celebrates the unsung heroes of cement production, namely the materials handling facilities, components, and machines that store, transport, and distribute fuel, raw materials, and finished products and thus keep the entire production process running. The issue begins with a review of storage solutions. With an article on pg 4 entitled ‘Massive Storage Meets Sophistication’ Dome Technology kicks off the feature by taking us through the design and construction of the enormous 160 ft tall dome at Lehigh Cement’s Mitchell, Indiana plant. The scale of the project, and specific customer requirements, meant that novel design solutions had to be employed in order to ensure success. Euromecc S.r.l then reviews a silo upgrade project from SOCOCIM Industries in Dakar (pg 10), and Henan SRON Silo Engineering Co. details an advanced powder mixing system and its benefits for storage applications (pg 15). Due to the nature of the materials involved, cement storage can be prone to various problems, including blockages. In this issue’s Silo Clean-out & Repair feature, Mole•Master (pg 19) provides an overview of the benefits of regular silo cleaning and maintenance; Aquajet (pg 23) takes us through a silo repair project in Spain, and Primasonics (pg 27) details the unique benefits of acoustic cleaners. Then, moving to our Conveying feature, BEUMER Group’s article ‘Ahead of the Curve’ (pg 30) introduces the company’s overland conveyor route planning software. The software is designed to generate a digital 3D model of a conveyor’s route in a virtual landscape during project planning; it does this more or less automatically, allowing a much faster planning process, and providing critical information to the customer at an early stage of the project. Also in the feature: Martin Engineering talk about the importance of adequate conveyor training and explain how it can boost both productivity and safety (pg 36), and the feature concludes with a round-up of recent product news and technology updates (pg 41). Moving on to the topic of Chains, this issue also includes an article from John King Group (pg 47) which details the process of optimising an elevator chain installation for an Indonesian cement producer. Up next is Bagging & Packing. In this feature, Cross Wrap Oy discuss ways in which the impact of freight and shipping costs for alternative fuels can be limited (pg 52), and Starlinger & Co. (pg 59) explain how modern cement packaging options can reduce the industry’s environmental impact. The issue then concludes with a focus on how the cement sector can reduce emissions and achieve the highest environmental standards: Bedeschi (pg 64) outlines a route to greener cement production through the development of novel solutions, and Scheuch (pg 67) marks the 10th anniversary of the company’s semi-dust SCR system. In other words, there’s lots of quality content and case studies to get stuck into – I hope you enjoy the issue. 3
Massive storage meets sophistication Rebecca Long Pyper, Dome Technology, reports on a recent collaboration between Lehigh Cement Company and Dome Technology to build the world’s second-largest clinker storage.
4
L
ehigh Cement Company collaborated with Dome Technology to build a clinker-storage dome in Mitchell, Indiana, USA, one that will increase operational capacity and take the company into the next decade of business. It is also the largest clinker storage in the Western Hemisphere and second in the world only to a Romanian structure that Dome Technology built in 2008. This dome, built for Lehigh Cement, a subsidiary of Lehigh Hanson, dwarfs most other bulk storage solutions, standing 220 ft in diameter and 160 ft tall. Its storage capacity
maxes out at 169 000 t, and three on-grade reclaim tunnels achieve 83% live reclaim. “It’s a colossal project. It’s one of our bigger domes as far as storage capacity,” said Dome Technology sales manager Lane Roberts. The project was centred around the second largest kiln in the Americas — an accurate representation of Lehigh’s “strong growth in the United States and continued commitment to our customers to meet the growing demand for a consistent, high-quality cement whilst improving our manufacturing efficiencies and reducing emissions,” said Lehigh Cement’s
Deputy Project Director and Civil Manager, Kevin Cove. Dome Technology’s scope of work includes dome construction, deep foundations, ring beam, tunnels, and at-grade entry for a front-end loader. While the dome size and sophistication are impressive, they simply represent a wider goal for Lehigh: reducing their environmental impact.
A green approach
The Mitchell project was part of Lehigh Cement’s efforts to upgrade an existing site 1.2 miles from the quarry, a proactive effort to reduce the facility’s impact on
5
the environment. Lehigh Hanson has pinpointed sustainability as a corporate value, and the strategy for achieving it is based on three pillars: environmental protection, social responsibility, and good corporate governance. That is the macro view, but success lies in the details. According to Cove, the Mitchell dome is large enough to replace work currently provided by five existing – and ageing – kilns and will reduce overall emissions to meet and exceed current EPA standards. “The clinker dome allows the clinker to be completely contained, vastly reducing particulate emissions or dust. Lehigh Hanson’s long-term success depends on sustainable business
practices as well as trusting relations with our neighbours, business partners and employees,” he said. Also, Lehigh has developed EcoCemPLC, a Portland limestone cement that meets ASTM C595 Type IL standards with more limestone, less clinker, and fewer CO2 emissions during production. It’s a new product that will be made and stored at the Mitchell plant, and to prove just how effective it can be, the company requested that the dome be built with it. Dome Technology put the material through considerable field testing prior to construction, and once confident, the crew sprayed 7000 cubic yards to form the dome. Application was seamless, and ECOCemPLC will be the material of choice for Lehigh’s future. “We wanted all of our new construction to use it to showcase its capabilities, including specialty applications such as shotcrete that was used for the dome,” Cove said. Even while under construction, the project drew public attention. The Indiana Ready Mixed Concrete Association recognised the Mitchell dome with an outstanding concrete award, and ENR Technology featured the project, highlighting its concrete Dome Technology recently completed a clinker-storage dome – the makeup that reduces energy second largest in the world – for Lehigh Cement Company in and emissions for a reduced Mitchell, Indiana, USA. concrete-carbon footprint.
Large dome storage: A new model
The large-scale site upgrade, including a new clinker storage dome, is one way that Lehigh Hanson is promoting environmental protection and social responsibility. 6
Lehigh leadership had precision on their minds when planning the project. They knew all their new clinker would be channeled through this single dome, so the structural and mechanical concepts had to be robust. More specifically, the total settlement had to be limited to less than 75 mm, and live storage capacity had to be a minimum of 140 000 t. A dome was a natural fit for these requirements. A dome is built with an unlimited lifespan, and its geometry, combined with the concrete shell, boasts World Cement BMHR 2022
CEMENT DISTRIBUTION
AUTOMATION SERVICES
CDM
AS
Cement Distribution Management Suite
Retrofit/ Greenfield
We make cement shipping smarter with end-to-end integration. In the last five years, over 8,000,000 cement trucks were loaded by PSCL’s Cement Distribution systems. Our goal is to reduce driver time loading at your plant or terminal, and to automate every step of the way with seamless integration into order and accounting systems.
The world leader in automation, logistics and quality monitoring solutions for the cement industry Work Smarter · pscl.com ®
Inside the dome, tunnels are installed on grade, then surrounded by structural backfill. Clinker will be layered on top and act as the dome ‘floor’.
unrivalled strength. Dome construction methods require no interior trusses, so the entire internal volume can be utilised for storage or reclaim systems. All domes offer ideal conditions for stored materials requiring a controlled environment. Seamless concrete construction, coupled with a membrane surrounding the entire dome, prevents water and moisture entrance. The dome’s insulated nature reduces heating and cooling of the walls and air inside, preventing condensation. Foam and concrete control humidity and moderate externally generated temperature fluctuations. A dome’s strength and geometry also provide a tolerance for differential settlement. Those qualities combined with geotechnical engineering and site analysis ensure proper foundation selection and performance. Lehigh’s list of ‘musts’ required focused and frequent conversation with the Dome Technology team. “Large storage domes are relatively new to Lehigh Hanson, so we required a high level of transparency with the design and construction techniques,” Cove said. “To ensure that we minimised issues with our feeding and withdrawal equipment, we needed to understand the total and differential settlements and balance the risks with cost.” According to Cove, Dome Technology suggested multiple options based upon finite element modelling that allowed for a cost-effective solution that would fit within equipment vendor tolerances to be found.
Systems and solutions
Increasing the height of the apex curb will allow the clinker pile to extend into the headhouse. 8
Lehigh Cement has operated the Mitchell site for years, but upgrading storage was tricky because a water-table issue prevented tunnels from being placed underground. World Cement BMHR 2022
However, tunnels built at grade would reduce extend into the headhouse, maximising interior capacity. So, Dome Technology suggested a space and saving Lehigh a significant amount new idea: Three tunnels could be installed on of money. Clinker “can peak up into the height grade, then surrounded by structural backfill to of the curb, which allowed them to achieve the within 1 ft of the top of the tunnels. tonnage,” Roberts said. “This was important The top foot was then layered with clinker, so we could get the angle of the conveyor that and this layer functions as the dome ‘floor.’ was needed but still achieve tonnage.” With the dome filled, the company could Soon the dome will be filled for the first expect 83% live reclaim through 10 drawdown time, and Lehigh Cement will begin to hoppers to the three tunnels, and any clinker realise all the benefits that this site was that remained between the troughs would designed to provide. serve as product reserve. Lehigh approved this Lehigh was completely satisfied with option because it met the capacity requirement the construction and has already hired for 169 000 t and 140 000 live t, plus a reserve Dome Technology1 for8/1/22 another project. WorldCementAd_Aug22_insertV1.pdf 5:53 PM of 29 000 t. Once operations begin, clinker will be reclaimed from the dome to the three tunnels that are elliptical in shape – 15 ft wide and 9 ft tall. From there it will be conveyed for processing as cement powder, and stored in existing concrete silos. The finished cement will then be trucked or railed to customers.
Collaboration to solve problems
Another challenge faced by Dome Technology was achieving the necessary capacity while dealing with a conveyor angle that could not change. Engineers determined the maximum angle for optimal conveyor performance, and fitting the dome within this configuration would not deliver the capacity Lehigh needed. Bumping up the dome’s diameter was the obvious, but unacceptable, solution. “We could have made the footprint larger, but that would have increased the cost substantially,” Roberts said. Instead, Dome Technology looked up – right to the top of the dome. The opening at the apex was increased in size, and its curb was made taller, stretching from the standard 2 ft to 10 ft tall. This will allow the pile to
C
M
Y
CM
MY
CY
CMY
K
Keep production rolling by ensuring kilns, silos, hoppers and chutes stay free of material buildup. hen bulk material stops moving due to accumulation or other obstruction, you have some serious and costly problems: unscheduled downtime, potential injuries, lost production, and diminished profits. The best way to clear buildup and ensure continuous flow is with Martin Engineering air cannons. Our cannons feature a new and innovative valve design that delivers more force with less air volume — highly effective with challenging wet and sticky materials. We invented low-pressure air blasting in the 1970s. With over 50 years of development, our cannons now deliver greater force output and more convenient serviceability. Don’t get stuck. With Martin Engineering as the solution to your conveying-related problems, you can maintain throughput, improve safety and reduce your overall operating costs.
For factory-direct service, training and sales call 1-309-852-2384 or to access our education programs and professional development options visit martin-eng.com and click the Learning Center tab.
GROWING WITH THE
10
REGION
Daniele Sciuto, Euromecc s.r.l., describes the technical solutions adopted to upgrade SOCOCIM Industries’ Rufisque cement plant in the Dakar region.
S
OCOCIM Industries, founded in 1948 as a private business under the name of ‘the Lime and Cement Company’ and then became SOCOCIM in 1978, has remained the historic flagship of the Senegalese and West African cement industry for more than 70 years. In August 1999, the factory became the property of the French group Vicat SA, which began a period of significant investment and modernisation. Today SOCOCIM Industries has the most important cement plant in West Africa, covering the entire national market and exporting more than 1 million t to various West African markets. This ensures total cement independence in Senegal and even makes it possible to largely satisfy the markets of neighbouring countries.
First approach
In 2020 the company decided to bolster its range of products by improving the capability of the packaging lines and introducing a new product to the portfolio. Euromecc supported the project by supplying a 2050 m3 storage silo with the relevant infrastructure. Euromecc had been approached by SOCOCIM Industries in December of that year. The company wanted a storage solution dedicated to a new product that they wanted to launch for sale. The business strategy had set the agenda, speeding up the whole process from RfQ to award. In fact, the purchasing process took only two months, and led to a supply contract being finalised in February 2021. Due to travel restrictions at the time, everything was discussed remotely, but was supported by a strong relationship built over the years with the VICAT group in France.
11
Design and construction
Due to limited space, items were pre-assembled in a dedicated area and then moved to site.
Euromecc's modular design allows for the installation of most of its components at ground level which can then be lifted into position. 12
With an early engagement focused on the needs of the client, mainly related to space and process, Euromecc designed a basic concept and layout. The starting model showed a Ø 12 500 mm silo, with twin-lane drive-through support structure aimed at not compromising the viability of the site. The storage unit was required to be fed from an existing pneumatic line, and meant to discharge onto bulk tankers and to the existing packaging line as well as have a pre-arrangement for a future opening in the discharge cone. Step by step, the design process moved over to the engineering, so that an adequate filtering unit was defined in order to de-dust the incoming pneumatic line. The final configuration was a 2050 m3 silo pneumatically fed with a 7000 m3/h dedusting unit, a flat discharge cone with a pre-arranged discharge on the side and three outputs delivering materials at 150 tph, serving the packaging equipment via airslides, the bulk loading station with a discharge spout accessible from the driver’s panel with a movable platform, and the possibility of a future big bag loader. The service floor under the cone is host to two high-efficiency blowers, where one operates as a spare unit, which aerate the five airslide sectors installed on the flat discharge area, as well as a 2500 m3/h filter which ensures the discharge operations are dust-free and keeps the discharge airslide with negative ΔPa, for a better flow. The whole system was then fitted with state-of-the-art indicators, sensors, process-valves, and HSE equipment according to the Vicat standards, including those related to painting which required a variant of standard C4 finishing, according to ISO 12944. As soon as every technical aspect was defined and agreed, the project went through the manufacturing process, which was carried-out with a special focus on the delivery sequence: due to the limited space available on-site it was necessary to spread the shipment over four different loads, so as to not to overcrowd the site and impact the installation. Furthermore, every container was designed in order to optimise the packaging and simplify the loading/emptying sequences and operations. Prior to dispatch, the material was inspected by a SOCOCIM representative, who visited the factory and checked the correspondence between the specification and the final products. This gave Euromecc the opportunity to show its highly-automated manufacturing process, where most of the tasks are executed by CNC equipment as well as robots for welding, sand-blasting, and painting. World Cement BMHR 2022
80 years handling bulk materials, globally
Round steel link chains Conveyor chains Central chains Mechanical chains Sprockets Wheels Components
CHAINS AND COMPONENTS FOR BULK MATERIAL HANDLING Telephone: (+39) 039.5320739 Email: cicsa@cicsa.com
www.cicsa.com
Installation
Top of the tanker can be accessed from a movable walkway, simplifying operations.
The installation was performed by local staff and coordinated by one of the Euromecc’s engineers, with global experience and knowledge of the bulk material’s storage and handling solutions. The main challenge of the project was related to installation: the new equipment was installed without stopping production, which had a limited assigned area of approximately 480 m2. Therefore, most of the engineering activities were carried out in an assembly yard 500 m away from the installation area – this allowed for large sections to be made ready for erection with a minimal interference on production. The silo positioning was carried out together with the staircase, allowing for the crane lift to be managed efficiently. Once the main unit was in place and safely accessible by staircase, the installation focused on devices and instruments; every motor has been wired to a lockable insulator-switch prior to going into a common junction box which represented the interface with the existing electrical plant at the factory. Despite the constraints and physical limitations, the silo was installed in less than 30 days, saving 14 days on the provisional schedule. Once it was completed, Euromecc arranged a training course over four days which was split into theoretical and practical sessions, attended by 40 staff divided into operations, maintenance, and electrical, in order to ensure the personnel were made aware of most of the specifications and routines on the plant.
Conclusion
The SOCOCIM factory upgrade was successfully commissioned in April 2022, ahead of the original time schedule. The project has presented challenges and required efforts like many others faced by Euromecc during its long-term presence in the market. Success was achieved due to the background built over time and the technical and operational skills developed from site to site.
About the author
After the silo was in place SOCOCIM looked after the connections with the production line. 14
As a sales and technical marketing specialist dedicated to Commonwealth and MENA regions for Euromecc srl, Italy, Daniele Sciuto is focused on the development of new projects from the feasibility phases for both independent private companies to larger corporations in the bulk materials industry. Daniele has a Mechanical Engineering background, and has been involved in the technical development, costing, and sales of several terminal projects all around the world since he joined Euromec 2012. World Cement BMHR 2022
Wen Peng, Henan SRON Silo Engineering Co., reports on the installation of an advanced powder mixing system installed for a Korean cement company.
he powder mixing system is a large piece of automatic production equipment. Compared with traditional mixers, SRON’s powder mixing system has a high production efficiency, a high degree of automation, practical structure design, safe and reliable operation, good homogenisation quality, high speeds, and accurate calculation. On the basis of incorporating the strengths of various similar products from other manufacturers, SRON has developed a new type of mixing system. The automatic control system, composed of an industrial control microcomputer and programmable controller, can mix powder materials (such as slag
powder, limestone powder, OPC powder, etc.) according to the required proportions, and it is widely used in various cement, mineral powder, and other mixing projects. This article looks at one of SRON’s EPC general contracting projects processing slag powder with a mixing system for a Korean company, focusing on introducing the powder mixing system’s core features.
Project overview
SRON’s powder mixing system has been installed to handle the Korean company’s slag powder storage and cement mixing project. The mixing system is an efficient and
15
Silos used in a cement mixing project.
3D image of a cement mixing project.
continuous material mixing system, which changes the moving speed and direction of the material ensuring that the materials are evenly distributed. This project is mainly composed of three parts: ff Storage system for slag powder, limestone powder and OPC powder. ff Mixing project for slag powder, limestone powder and OPC powder. ff Feeding system for finished cement. The storage system consists of three steel silos, of which the specifications are: slag powder silo Ø 5 x 7.5 m (straight cylinder), limestone powder silo Ø 5 x 5.0 m (straight cylinder), OPC powder silo Ø 7.2 x 13.2 m (straight cylinder), all using centre discharging fluidised gravity technology. The materials stored in silos are: 150 m3 of slag powder, 100 m 3 of limestone powder and 600 m 3 of OPC powder. The storage system consists of a steel frame structure, steel silo body, lifting equipment, feeding equipment, discharging system, dust removal equipment, and other auxiliary systems. Among them, the discharging system includes a fluidisation system, roots blower, air supply pipeline, and control valve, etc. The mixing system of slag powder, limestone powder, and OPC powder consists of a double-rotor weighing scale (manual screw gate valve, rotor feeder, and rotor scale), air chute, chute fan, mixer, dust collector, and other auxiliary systems. The feeding system for finished cement consists of the following: elevator, air chute, chute fan and other auxiliary systems.
Process design
Display of mixing process equipment.
The materials from different silos are continuously discharged into the chute from the discharge outlet in different proportions through a quantitative feeding scale monitored by the control system, and then transported into the mixer via the chute in order to be mixed. At the same time, efficient dust removal and gas balance systems are equipped to ensure stable and reliable operation of the system.
Storage and cement feeding systems
Process flow diagram for cement mixing. 16
The slag powder is conveyed from the silo into a mixing system by a silo bottom discharge device and an elevator. The feeding operation World Cement BMHR 2022
of the slag powder silo, limestone powder silo, and OPC powder silo is completed through ash pipelines. On the top of the silo, a dust collector can ensure that there is no dust escape during the feeding process so as to meet environmental protection requirements; natural ventilation holes or safety valves can adjust the pressure between the inside and outside of silo; a radar level gauge can monitor the materials in the silo; and a radio frequency admittance material level switch is used for material level alarm. All three silos are conical steel silos with a cone angle of 55˚. When the gasification air is fed into the silo, the materials in the silos are fluidised, and are then mixed and homogenised by gravity during their downward movement. Finally, they enter the discharging port to be discharged.
Working principle of the powder mixing system
The materials discharged from the slag powder silo, limestone powder silo, and OPC powder silo are weighed by a double-rotor weighing scale first and then enter an air chute. Under the fluidisation of the chute fan, they finally enter the mixer. There are three air cannons under the limestone powder silo, which can release materials when they are compacted. During the conveying process, dust collectors installed at the dust flying points start to collect dust so as to meet environmental protection requirements. The mixed, finished cement is lifted by an elevator and conveyed by the air chute, and finally enters the first phase in the cement silo.
Design software for pneumatic conveying systems Need help with designing or troubleshooting pneumatic conveying systems? PneuCalc is the only software application that can optimize your design while avoiding pitfalls. Better design systems in a fraction of the time!
Comprehensive
Analyze
Time saving
Intuitive
Cost effective
Robust
Advantages of advanced mixing technology
SRON’s mixing technology solves the problem of poor material discharging in the mixing system. The batching rotor scale is used for precision control, which ensures a stable and accurate supply of materials. The mixing system has accurate material batching, uniform mixing and operates quickly so that it maintains continuous production and a large handling capacity. Also, it can be used alone or online with a variety of other equipment. Excellent design and strict quality control are the guarantees for the success of a project. SRON’s quality inspectors were able to overcome a number of obstacles and visit the factory area to inspect all equipment parts in accordance with the company’s quality management process, ISO 9001
Let PneuCalc help you reach production capacity and improve your bottom line! Save time and download a free demo today. pneucalc.com
5, Place Ville Marie, bureau 1400, Montréal QC Canada H3B 2G2 Tel: +1 438 320 2113 | pneucalc-info@hatch.com
Packaging of dust collector steel supports.
Construction process of spiral silo.
Overall effect display of spiral silo construction. 18
quality control procedures, and design requirements. As such they carried out a raw materials inspection, equipment manufacturing process inspection, and factory inspection to ensure the reliability of products. All equipment and material inspection data were archived to ensure that every part was well documented. SRON carefully packed the equipment before shipment to ensure that the products were not damaged during long-distance cross-border transportation and loading and unloading operations. During the construction process, the remote support of professional engineers was also essential. The steering group composed of structural, technical, and electrical engineers, and SRON’s building technicians provided technical support for various problems during the installation process. On site, professional engineers provided construction guidance, allocated project resources, and conducted an on-site supervision of equipment use, material quality, and construction quality. Each member of the construction personnel is a skilled worker with professional qualification certificates. In addition, daily and weekly construction schedules and summary reports were produced to ensure construction quality and progress. A scientific and reasonable construction plan is the basis for ensuring the efficient and orderly implementation of any project. In view of the construction of this slag powder and mixing system, the installation engineers of SRON’s engineering department and their chief engineer carried out a meticulous study of the designs. The project manager led the project construction in strict accordance with SRON’s construction plan, and finally completed the construction of the slag powder and mixing system project, which was highly praised by the owner. World Cement BMHR 2022
GETTING THE MOST OUT OF YOUR SILO Jeremy Snyder, Mole•Master, provides an inside look at the benefits of silo cleaning and maintenance for a cement processing facility.
C
ement manufacturers are sometimes reluctant to invest in a regularly scheduled cleaning and preventative maintenance programme for their processing facilities, instead opting for an 'If it ain’t broke, don’t fix it' approach. While the appeal of staving off cleaning and maintenance expenses is understandable, the ramifications can be less obvious and very costly. The difference between avoiding a shutdown and recovering from one reveals the true ROI of scheduled silo inspection, cleaning, and maintenance. Delaying the inevitable can mean a drastic reduction in operating capacity and salvageable material.
19
Build-up happens in all silos over time. Many factors – including the climate, the condition of the material, and storage times – affect the rate at which the material hydrates. A cement silo with seemingly little-to-no reduction in capacity can be deceptive. Once capacity begins to decrease, it is lost at an escalating rate over an increasingly shorter period of time. Material that could have been salvaged and sold to help offset clean-out costs must instead be written off.
Mole•Master crews travel with a full complement of safety and cleaning equipment to tackle any silo maintenance challenge.
Silo inspections include wall soundings conducted by a professional structural engineer. 20
Background
A New York based cement processing company recently learned that not having a regular silo cleaning and maintenance programme in place can present unintended and unanticipated consequences. The company was faced with unsalvageable material and a much larger investment necessary to return the facility to full capacity and production. This cement company turned to Mole•MasterTM for a finished cement silo clean-out project focusing on an approximately 50 year old, 175 ft tall cement storage silo with 20 in. thick walls. The inverted-cone type silo had a nearly 20 ft long discharge opening at the bottom and numerous windows around its outside edge. A 3 x 3 in. side access door was located 15 – 20 ft from the ground. There were no additional access points and no scaffolding. The silo had not been emptied for at least 20 years, and all the stored finished cement was thoroughly hydrated. Storage capacity was reduced by nearly 80%, resulting in a complete loss of production. Having unsuccessfully attempted to complete the project internally, the company called in two outside contractors. The scope and complexity of the project proved too challenging and their efforts were ineffective. A plan was briefly considered that involved prefabricating the bottom of the silo (at a cost of nearly US$2.5 million), but instead the decision was made to contract Mole•Master.
Getting involved
Mole•Master technicians soon realised that the silo needed a complete clean-out as it was full of non-flowing cement and there was no movement of material through the discharge outlet. The crew also identified additional problems that needed correction. More than 2500 t of hardened cement had to be removed from the silo, which could not be completed utilising human entry due to safety concerns. The silo clean-out technicians used a range of specialised tools to complete the work without hazardous human entry of the storage silo. Mole•Master’s crew did not know whether or not the air slides were functioning and recommended repairing them as well as making a number of other repairs and modifications at their initial time estimate of 45 days. Further inspection revealed a far greater degree of hardened material than initially thought. The first task was to create a safe environment so that cleaning could be performed. Mole•Master used a combination of bottom and top clean-out, employing the Safe-T-ShotTM system to perform carbon dioxide World Cement BMHR 2022
W E
C O N V E Y
Q U A L I T Y
Expertise in the Cement Industry • Quality and Reliability for kiln capacities up to 12,000 t/d • Proven by nearly 24,000 references worldwide
AUMUND Foerdertechnik GmbH cement@aumund.de · www.aumund.com
blasting, and the Big•MoleTM system that is used for projects that present the highest level of difficulty. The Safe-T-Shot system dislodged enough hard cement to gain entry to the side access door, through which the crew vacuumed loose cement. The cleaning process created a significant amount of dust which had to be contained with a block of tarps positioned across the space between the cement silo and an adjacent silo.
Regular silo maintenance and cleaning: cost versus investment
The cost of regularly scheduled silo cleaning, maintenance and repair can be offset by freeing up storage space and preventing valuable inventory loss. In turn, freed-up storage space allows a cement manufacturer to operate more cost-efficiently by running the production plant at a uniform output. Reducing production during slow times and increasing production when sales pick up reduces efficiency and profitability. Running a plant at a uniform output requires sufficient silo storage capacity to house inventoried product. By keeping silos clean and ensuring that their planned storage capacity is maintained, a cement plant can be operated at maximum uniform output. Despite the reluctance on the part of cement processing companies to invest in equipment that is not yet broken, the rationale for doing so is clear: Allocate money for regular silo cleaning and maintenance to avoid the loss of cement storage space, which slows down production and results in less product sold, and stored product that has deteriorated due to hardening and can no longer be salvaged. The downtime in production also underscored the true value of storage capacity; 5000 t of capacity to hold new, undamaged cement could have a market value of more than US$3 million.
Cleaning and maintenance programmes
Mole•Master technicians regularly inspect all cleaning and safety equipment to ensure every job is completed safely and successfully.
Mole•Master silo cleaning and maintenance programmes are available as turnkey services or as do-it-yourself projects using the Junior 360˚TM, Arch•MasterTM or Safe-T-Shot equipment purchased or rented from the company. A successful maintenance programme should be paired with regular inspections to ensure internal and external structural issues are detected and repaired before they become serious problems.
About the author
Mole•Master mobilises anywhere in the world to tackle the most challenging silo and inspection projects. 22
Jeremy has more than 15 years of industrial cleaning experience with a background that includes media blasting, oil and gas, and construction operations. He manages silo cleanout, inspection, and sanitation projects in a variety of industries including grain, cement, food processing, and manufacturing. World Cement BMHR 2022
Silo repair in Spain Aquajet details a successful silo repair project for a cement plant in La Robla, Spain.
D
uring an annual maintenance shutdown, a cement plant in the village of La Robla, Spain, needed an effective way to repair a 100 m tall, 16 m diameter concrete silo used to store raw materials. Similar to many silos built in the 20th Century, the walls of the vessel were
held together with rebar on the outer and inner layers of concrete. However, with age, deterioration had occurred and concrete began to fall away. In 2019, the cement plant hired a company specialising in concrete and structure repair to fix the silo.
23
The hired crew used hand lances to remove the deteriorating concrete and scaled the silo with a scaffolding system to reach higher areas. Unfortunately, the crew was only able to repair the lower portion of the silo with the limited time they had, which put the remainder of the repair on hold. When the project resumed two years later, Jose Rodriguez was hired to complete the repair. Rodriguez had been involved in the initial stage of repair and had since started another company, Fixen Structural Services, with a focus on structural reinforcements and repair. Fixen proposed using Aquajet’s Ergo Hydrodemolition robot to complete the challenging repair on budget and ahead of schedule.
The project resumes
Fixen Structural Services proposed a new hydrodemolition technology over hand lancing to repair the deteriorating concrete of the silo.
Fixen Structural Services was established in 2019 to provide structural repair and reinforcement for large structures, such as silos and bridges. The company, based in La Rinconada, Sevilla, Spain, works on projects across the globe and emphasises the importance of power and simplicity in its projects in order to provide customers with the best possible results. Since investing in Ergo in late 2020, the Fixen team has been impressed with its quality, speed, and accuracy. The equipment works as a replacement to hand lancing, with the ability and precision to complete repairs within a limited work space. The method is also safe and cost-effective with a compact and lightweight design that offers versatility for a variety of repair projects. The Ergo hydrodemolition robot, which works with a climber that attaches to any standard scaffolding pipe and moves along it, provides four times the power of a hand lance. Exerting 1000 N of reaction force, the Ergo removes concrete or other material to a consistent preset depth. The equipment is ideal for working on vertical vessels. Fixen currently has two Ergos – one used as the primary machine and the other as a back-up unit.
High stakes
The robotic hydrodemolition method along with the use of hanging platforms allowed the work to be completed by the deadline. 24
The cement plant’s maintenance shutdown had a deadline of four weeks, so it was critical to complete repairs quickly. Because of his previous experience working on the silo and knowing the scope of the project, the plant managers approached Rodriguez and asked if Fixen could reinforce and repair the silo. Fixen proposed a robotic Hydrodemolition method along with the use of hanging platforms to complete the work by the deadline. Traditional hand lancing for concrete repair could take up to 24 hours of non-stop work with a full crew of workers for four weeks or longer. World Cement BMHR 2022
AGUDIO: INNOVATION THAT SHORTENS DISTANCES.
FLYINGBELT, CABLE CR ANES, MATERIAL ROPEWAYS, CUSTOMIZED CABLEWAYS. Since 1861, reliability, performance and innovation have been our values. Agudio is a leading brand in engineering and construction of rope-hauled material transportation systems.
Cable cranes
Material ropeways
Flyingbelt
Dust suppression
Flying over obstacles, since 1861 LEITNER S.p.A. - Leini Office - Via Tommaso Agudio, 8 - 10040 Leini - Torino - Italy - Tel +39 011 997 33 55 -www.agudio.com - info@agudio.com
Fixen promised that a repair could be completed within four weeks using the Ergo system.
Completing the silo restoration project
The repair team were equipped with practical knowledge of hydrodemolition and the Ergo.
The silo restoration job took place September 2021, two years after Rodriguez had worked on the first stages of the project with his former company. The silo had a total of 32 sections to repair, each 45 m long. The Fixen team connected the Ergo to an electrical hoist to reach the areas of repair. The team first used the robot to cut and remove the silo’s deteriorating concrete and then installed stirrups to anchor the existing horizontal rebars and attach them to the concrete. The final step of the repair was to fill the open spaces with fluid mortar to complete the section. The team achieved a production rate of one metre per minute, removing two 45 m vertical sections of concrete each day. A crew of two removed a total of 1440 m of concrete and finished the job with two days to spare. However, there were some challenges. With the silo’s height of 100 m, rather than using a traditional scaffolding system, the Fixen team decided to opt for a safer motorised hanging platform to comfortably stand on and bring additional equipment up with them as they worked on the structure. Additionally, the crew needed approximately 100 m of constant water pressure to ensure a successful hydrodemolition repair. To achieve this, a 2500 bar Hammelman pump with a flow rate of 24 l per minute was used. The pump, situated on the ground for the duration of the project, incorporated a 120 m long, 3000 bar pressure, hose extending up the structure to the Ergo. The Ergo controller was placed on a hanging platform, following the Ergo climber on each 4 m vertical section. The cement plant provided the water and discarded the blast water into a cistern on-site.
Forming a partnership
Aquajet distributors are located across the globe, offering hydrodemolition contractors training, consultations, machine parts, and customer service. Fixen’s local Aquajet distributor is Hammelmann SL, a company Rodriguez has had a relationship with for about a decade. The companies have worked together on training, equipment, advancements, and best practices.
Overcoming limitations
Fixen Structural Services completed the silo repair using the Aquajet Ergo. 26
Equipped with practical knowledge of hydrodemolition and the Ergo, Fixen was able to repair the silo and complete the job, providing the cement plant with a cost-effective and lasting solution. World Cement BMHR 2022
Primasonics describes the role of acoustic cleaners in preventing material build up and maintaining continuous flow in the cement silo.
KEEP IT MOVING! A
coustic cleaners, also known as ‘sonic sootblowers’, are widely employed wherever ash, dust and powders are generated, processed, stored or transported. Primasonics’ acoustic cleaning systems ranging from 60 – 420 Hz in fundamental frequency, have been beneficial in both preventing material hang-ups and maintaining continuous material flow in a range of industrial processes including silos and hoppers. Indeed, some of Primasonics’ most challenging but successful applications were within silos which contained dry materials such as cement, carbon black, and fly ash to name a few
common examples. It is important to understand several main advantages that acoustic cleaners have over alternative cleaning and materials handling methods which have been employed to try and aid material flow. Primasonics’ acoustic cleaners operate at fundamental frequencies much higher than the natural frequency of the silo construction, thus preventing resonance leading to vibrational/structural damage. Instead, sound at an extreme pressure level is focused into the bulk material directly, which is used to break the adhesive and cohesive bonds between the bulk
27
material particles and the walls of the application. This is quite unlike vibrators which by their very nature and method of installation cause vibration and stress weaknesses within the vessel or structure to which they are attached. The vibration resonances from the vibrators first have to pass through the vessel wall before reaching the material. With the acoustic cleaner, the sound is not used to ‘drive’ the vessel with 100% of the sound energy focused into the material itself. Primasonics’ Audiosonic acoustic cleaners aid material flow from hopper and silos in industries including, but not limited to, cement, gypsum, carbon black, MDF and other wood products, chemicals, food, pharmaceuticals, and power generation plants. They are also employed in a range of ancillary plants such as baghouse filters, cyclones, ID fans, ductwork, as well as extreme temperature boiler applications for steam/power generation plants. Air cannons/blasters seek to provide a very localised cure for a blockage problem which has already occurred. In many cases, the air cannon simply ‘blows’ a localised hole through the blockage, necessitating the installation of many air cannons within the general problem area. This differs from acoustic cleaning, as the problem is approached with a totally different philosophy – by preventing the build up from occurring in the first place. Acoustic cleaners are very simple to install by either using Primasonics’ standard connecting flange, mounting tube assembly, or custom mounting arrangements specifically designed to suit the application. The fundamental frequency and therefore model required along with the quantity are determined on a case-by-case basis dependent on a number of factors and parameters within the application itself. A dimensional drawing outlining each elevation of the application along with a specific questionnaire are requested prior to being able to quote. The possible mounting positions are also considered when calculating the unit(s) required for effective coverage.
How do acoustic cleaners work in silos and hoppers?
Primasonics Audiosonic Acoustic Cleaners are simple in their operation, requiring only normal plant compressed air for their initial energy source. Compressed air enters the wave generator and forces the only moving part, a high-grade titanium diaphragm, to reverberate very rapidly within its specially designed housing. These rapid reverberations set up the standing sound waves which are then amplified from the base tone to the selected key fundamental frequency set by the bell section itself. The current range of models 28
produce set fundamental frequencies between 60 – 420 Hz.
The 3 key storage problems Bridging Irrespective of whether the bulk storage facility is under 500 kg or over 10 000 t capacity, Audiosonic acoustic cleaners can be used to eliminate the three key problems that occur in silos. The first of these is ‘bridging’, which is caused by when the design of the conical section has an insufficient angle of repose, side walls with excessive frictional properties or an insufficiently sized outlet for the material being contained. Consequently, these problems can become severe if a silo is used for materials other than those it was designed for, either through changes to the process or plant layout over time. To combat bridging, an acoustic cleaner is mounted close to the outlet just underneath where the bridge is known to typically form. When the unit sounds, single particles and clusters of particles move at different speeds, causing the bridge to collapse and restoring the material flow. Once the acoustic cleaner has ceased to sound, new bridges will begin to form. To counter this, the sounding may be controlled in one of two ways, either simply on a timer device typically set for a few seconds every 5 – 10 minutes during material discharge only or alternatively it can be controlled automatically via a flow sensor downstream of the outlet or even from load cells. Ratholing or funnel flow The next problem associated with material build up in silos is ‘ratholing’ or ‘funnel flow’, which as the name suggests is material adhering to the sidewalls causing reduced working capacity within the silo itself. This usually occurs with material that displays mechanical interlocking properties or very quickly bonds without compaction, for example by means of solvent evaporation. To defeat ratholing, acoustic cleaners with a long wave length are placed on the top of the silo, usually through an available existing manhole or inspection hatch. If there is a large amount of hardened material that has built up over an extended period of time, then the silo should be cleaned offline prior to the installation using a cleaning method such as the GyroWhip system. This is because if an acoustic cleaner were to be sounded in a silo with these thick hardened build-ups, and the adhesion forces between particles were greater than those between the side walls of the silo, there may be a chance that the material could become dislodged in slabs and cause an obstruction to the outlet. This is due to the power of the low frequency acoustic cleaners which continue to sound their transmission through the bulk material until the reflective surface of the World Cement BMHR 2022
silo is reached. When considering a full silo which is prone to ratholing being slowly discharged and emptied, one can imagine the central core of the material lowering a small amount while an outer ring close to the side walls remains at the same height. Without acoustic cleaning, this process would continue until eventually the central core would be discharged and the outer ring would be left adhering to the side walls. The control engineer must determine whether to remove the silo from active process lines while offline cleaning takes place, or to refill the silo and risk lower control over the quality of product as older adhered material mixes with new material entering the silo. When using acoustic cleaners, once the central core has lowered slightly, the cleaner will sound and the bonds holding the outer ring of material will collapse. This will form a flat surface along the top of the material in the silo. This pattern is repeated as the silo empties, even if the silo refills before complete discharge has taken place. This now allows a ‘first in, first out’ mass flow pattern. Again, the acoustic cleaner can be controlled by a simple solenoid valve and timer arrangement or via PLC of central DCS system. Cross contamination The third area in silos and hoppers where acoustic cleaners can be employed is in preventing material batch cross contamination. Take the example of a weigh hopper, sometimes not all material is discharged before the next batch enters. This can lead to product contamination, which can in turn lead to quality control problems. The reasons for material failing to discharge from hoppers are similar to those already mentioned, but in weigh hoppers or similar batch filled vessels, an additional problem occurs. Material can make contact with cold side walls and moisture precipitates from the bulk material onto the side wall. This moisture forms a meniscus between the side wall and the particles which holds the powder in place so that even after discharge, a thin layer of powder remains. In this instance, the acoustic cleaner is activated when the bin is being emptied, and the alternate compressive and rarefactional forces break the surface tension of the moisture. This allows material to flow out, leaving the vessel to completely empty.
SAFER CONNECTIONS. BETTER PERFORMANCE.
Exclusive and quick field connection link • Safer installation • Faster maintenance • Easier field connections
Summary
Acoustic cleaning systems are extremely low maintenance with the only consumable part being an aerospace specification titanium diaphragm, which should provide a minimum of two years uninterrupted service before requiring replacement. This is then a very simple and short task taking approximately 10 minutes to remove and replace and can usually be undertaken while the system remains online with the acoustic cleaner isolated.
To learn more and schedule a demo, scan the QR code or visit:
regalrexnord.com/RexPro Regal Rexnord, and RexPro are trademarks of Regal Rexnord Corporation or one of its affiliated companies. © 2022 Regal Rexnord Corporation, All Rights Reserved. MCAD22046E • Form# 10514E
Creating A Better Tomorrow
AHEAD OF Dr. Andreas Echelmeyer, BEUMER Group, outlines an innovative planning method for curved overland conveyors designed to provide customers with a high efficiency, long distance conveying solution.
H
ow can cement plants make their operations more sustainable to reduce their environmental footprints? One element that can be suitably adapted to match the conditions is the efficient transport of limestone. Overland conyeyors that can move large quantities of material over long distances from the quarry to the plant are required. BEUMER Group relies on modern planning and layout tools to support operators at an early stage of the project and design the ideal conveying solution together with the customer. BEUMER Group installed the first overland conveyor with horizontal curves as early as 1969. Since then, calculation methods and components such as idlers, belts, and drives have undergone constant development, resulting in the implementation of increasingly efficient conveying systems for routes that are often complex. Cement manufacturers can use BEUMER’s curved, troughed belt and pipe belt conveyors to transport raw materials over routes with steep inclines and narrow curve radii. “We can exactly match our systems to the required conveying task and topography,” says Dr. Kilian Neubert, Global Head of Mining at BEUMER Group. “We rely on state-of-the-art planning tools to provide our customers with an efficient, sustainable, and cost-effective material flow.”
Sustainability in the cement business
As important as limestone is for the production of cement, quarrying has far-reaching effects on the environment and society.
30
RV CU E
THE
31
The topography of the existing terrain has a significant influence on the design of the conveying system.
Long and difficult conveyor line distances must be considered during the planning phase.
A 3D model of terrain and conveyor: the advantages of earthworks (cut & fill) or steel structures [top] can be quickly and precisely assessed using graphic representations and mathematical calculations [bottom]. 32
This is why cement manufacturers constantly strive to make their extraction and processing operations even more efficient and sustainable. It is especially important for efficient transport of limestone over longer distances, that environmental compatibility of the complete plant is improved. This is achieved by optimised routing and the selection of suitable methods.
The fundamentals and capabilities of modern conveying systems
No two conveying systems are alike, even if the primary task of transporting material from A to B appears comparable. “We must adapt the components and the system to the material to be conveyed,” says Neubert. “The mass flow to be conveyed and height differences that need to be overcome over the length of the conveyor line are important factors that we must address when designing a system.” The energy consumption of long, horizontal belt conveyors is primarily determined by the main resistance in the upper and return strand in stationary operating conditions. This resistance consists of the running resistance of the idlers, the indentation rolling resistance, and the flexing resistance of both the conveyed material and the belt as they run over the idlers. The forces required to overcome these resistances depend on various operational and design parameters; however, they can be determined using the ‘single resistance method.’ If components with low running resistances are used, such as belts with reduced indentation rolling resistance or running-optimised idlers, the calculations for systems nowadays show considerably lower tractive forces for the belt than those of a few years ago. This leads to lower energy costs, and smaller radii can also be selected for the horizontal curves due to the lower tractive forces of the conveyor belt. The topography of the existing terrain also has a significant influence on the design of the World Cement BMHR 2022
The answer to your bulk handling questions Ship unloaders
Road mobile ship unloaders
Storage & reclaim
Convey units
Truck loading
Ship loaders
www.vanaalSTbulkhandling.Com
conveying system. An in-depth analysis of various dynamic load cases and a thorough investigation of the technically feasible horizontal and vertical curve radii must be conducted to design the system in the most efficient and environmentally friendly way. This is especially true for longer and more difficult conveyor lines. Potential obstacles that must be considered during the planning phase include residential areas, roads, and rivers. “Today, we can design curved overland conveyors of up to 20 km or longer without the need for a transfer tower,” says Neubert. The conveying capacities of a system like this are more than 20 000 tph.
The right layout
planning, more or less automatically.” The critical topography data can be provided by customers, or drones are used to capture terrain data. Important factors such as ‘cut and fill’ volumes, i.e. the necessary excavation work, and the required steel structures for the conveyor can be evaluated and illustrated on this basis. “This procedure considerably accelerates the project planning process and enables us to provide project-critical data to the customer at an early stage of the project,” says Neubert.
Ongoing development in conveying technology
The 1990s saw BEUMER Group start its development into one of today’s leading suppliers of pipe conveyors. In these systems, the idlers form the belt into a closed pipe that protects the material to be transported against external influences and the environment from emissions such as dust and odours. This conveying solution is therefore ideally suited for fine bulk materials such as ore concentrates. Pipe conveyors also allow tighter curve radii and greater angles of inclination compared to conventional troughed belt conveyors. However, what if bulk material with large grain sizes requires a larger The BEUMER Overland Layouting Tool generates a digital 3D pipe diameter? The rule of thumb model of the conveyor in the virtual landscape during project here is that the pipe diameter should planning – almost automatically. be about three times the maximum grain size. To solve this problem, the BEUMER Group developed the U-shape conveyor. “This variant combines the advantages of a troughed belt conveyor with those of a pipe conveyor,” says Neubert. The idlers form the belt into a U-shape rather than a pipe. The U-shape conveyor enables tighter curve radii than a troughed belt conveyor, higher These 3D visualisations are also ideal for supporting PR work. mass flows than a pipe conveyor, and also protects the conveyed material from environmental influences and the environment from material loss and emissions. “We use our BEUMER Overland Layouting Tool to ascertain the ideal layout for the system,” says Neubert. “It generates a digital 3D model of the conveyor in the virtual landscape during project
About the author
No two conveying systems are alike, even if the primary task of transporting bulk material from A to B appears comparable. 34
Dr. Andreas Echelmeyer, Director Conveying & Loading Systems at BEUMER Group is a long-term Expert in Conveying & Loading System with focus on Bulk materials handling. Working at BEUMER Group since August 2015. He was employed in the steel industry for eight years, after which he worked in plant engineering for twelve years. World Cement BMHR 2022
“SUITED FOR HARSHEST CONDITIONS” DISCOVER A HUGE PRODUCT RANGE OF A LEADING MANUFACTURER OF CONVEYOR CHAINS AND SPROCKETS – SINCE 1925. Central bucket elevator chain with forged link plates
Sprocket with noise reduction technology
Reclaimer chain with SCS PO and HE-Roller on a Click-On Mounting System
Cutting-edge chain technology Designed & manufactured by KettenWulf www.kettenwulf.com
36
Jerad Heitzler and Todd Swinderman, Martin Engineering, talk about the importance of conveyor training as the key to successful bulk handling.
A
s with many types of industrial equipment, one of the most important elements of safe, efficient conveyor operation is proper training. Bulk handling conveyors are typically massive, powerful systems that can move tons of material per hour, often in complex networks and over long distances, thereby minimising costs while performing work that would otherwise create labour and logistical nightmares. But their size, speed and power also present the risk of a catastrophic injury that can occur in the blink of an eye. Even the reaction time of a highly-trained professional athlete is no match for a bulk material conveyor. Conveyors apply large amounts of mechanical energy to what is essentially a giant elastic band, stretched tight and threaded through a maze of components. This stretched band is often loaded with tons of material, sometimes using drive motors as large as 600 HP (450 kW). A typical conveyor belt moves at a relatively constant speed, commonly running between 0.5 to 10 m/s (≈100 to 2000 ft/min.). Given the weight, speed, inertia and kinetic energy, enormous forces are involved. The human body, able to generate less than 1 HP (0.75 kW), simply cannot compete.
Training challenges
One of the challenges facing conveyor operations is the loss of expertise and knowledge as seasoned, experienced employees retire. A deep understanding of how conveyors function may not be handed down through the basic on-the-job training that is passed from worker to worker. Although valuable, this type of training cannot be vetted to be sure that the underlying plant concerns are understood by a learner, nor does it allow for adjustments that may need to be considered with changes in production or auxiliary equipment. Furthermore, information that is transferred to new employees may not reflect industry best practices. When plants take a ‘here’s how we do it’ approach, they are vulnerable to past workers teaching techniques that may not be the best long-term resolutions. This introduces risks to the plant in terms of safety hazards, inefficiency and premature equipment failure. In many plants, there is a lack of qualified conveyor trainers. Most conveyor training comes from vendors of systems and components. Suppliers can train very well on how their products should be maintained and installed and what problems they can solve. But much of this type of training is done from the vendor’s or manufacturer’s own point of view. Rarely is training available that addresses the plant or mine personnel’s perspective.
37
This can tarnish training effectiveness, reducing the learner’s interest if it does not speak directly to their recognised needs. There are also generalisations that are accepted as truisms and seemingly require no proof due to their long-standing use in conveyor operations. It is easy to perpetuate bad habits unless operations personnel have solid, real-world knowledge in bulk material handling and can make educated decisions when addressing problems. With the experienced operators who developed and handed down these practices now fast approaching retirement, there is a need to provide knowledge to the younger operators and maintenance workers in order to avoid the trial
Conveyor drive motors can be as large as 600 HP (450 kW), moving belts as fast as 2000 ft/min. (10 m/s).
Bad habit: factory-trained specialists will help operators avoid risky behaviours.
The most effective way to reduce fatalities is to minimise unsafe behaviours. 38
and error associated with applying many of the handed-down approaches. While loss of ‘tribal’ knowledge is an issue, it also creates an opportunity to significantly improve operations through third-party expert training. Factory-trained specialists who focus on overall conveyor performance and safety rather than just component function can deliver thorough, objective instruction that is untainted by a ‘we’ve always done it this way’ approach. Training based on a combination of deep industry experience and modern engineering will greatly improve operating decisions, resulting in higher productivity, fewer safety incidents, and reduced unplanned outages. Dealing with complex and changing regulations can present additional challenges. Some regulations may not fully protect a worker, depending on an individual plant’s circumstance, so states and corporations often add their own requirements in an effort to improve productivity and minimise injuries. Furthermore, new conveyor systems are increasing in size, speed, complexity, and sophistication, with automation playing an ever-increasing role. The move toward automation was originally targeted at reducing labour costs but is now focused more on productivity improvements. As systems start to ‘run themselves’, the reasons for unplanned shutdowns can be misunderstood and not addressed, and systems may be bypassed, resulting in going back to the same old procedures. Maintenance is becoming more driven by data knowledge and less by practical experience. Updated design and control philosophies are becoming more critical for making informed operating and repair decisions, and conveyor operators and maintenance personnel are increasingly in need of a deeper understanding of the entire system. All of these factors indicate a need for training that is specifically tailored to individual sites and operations. The one-size-fits-all approach is becoming less attractive – and less effective – with each passing year. Understanding how and why accidents happen is also critical in preventing them from occurring. Some might argue that workers’ unsafe acts are the primary cause of accidents. Yet many safety professionals have realised for some time that the root causes of accidents are not that straightforward. Often, the employee’s action is not the only – or even the most significant – root cause. The real underlying causes are usually more involved and require a more complete accident analysis, followed by thoughtful corrective action. Addressing the symptoms with workable long-term root cause solutions will reduce unsafe practices, improving availability and safety, while enhancing profitability. A 2003 study by a major corporation found a correlation between fatalities and unsafe practices, indicating that for every fatality there are an estimated 300 000 unsafe behaviours. World Cement BMHR 2022
In search of a deeper understanding
Most operations personnel are only expected to know the basics of how conveyors operate, and they may not be fully aware of their limits, safety protocols, or best maintenance practices. Optimising a conveyor system requires an advanced understanding of how fugitive material relates to safety and the newest technologies to control dust and spillage, as well as accommodating changing production demands and how to use existing designs to meet those demands. Some plants lack a deeper understanding of equipment limitations, which encourages workers to treat symptoms such as fugitive material by adjusting skirt seals, for example, when the real culprit may be insufficient belt support or wear liners. Equipment vendors and third-party trainers can be a highly effective source of training, but there are hundreds of companies providing such services, and their expertise and approaches vary widely. Most are not bulk handling specialists, and even among those that focus on conveyors, their offerings are rarely plant-specific. That means the nuances of an individual facility and its equipment are addressed by a generic programme presented to all bulk handlers. Training is often piecemeal, with little follow-up to evaluate progress toward plant-specific goals and spotty access to industry experts. Some firms take training seriously, yet fail to repeat and update training often enough. Any approach that allows maintenance personnel to drift back toward trial and error learning is certain to increase costs and reduce effectiveness. The results can include a lack of deep understanding of the plant’s conveying systems and how the various components should work together, as well as increased regulatory oversight, disengaged workers, reduced productivity, poor safety records and increased labour turnover. In contrast, dedicated educators with a specific focus on (and a reputation for) expert conveyor training will guide personnel along a path of best practices and continuous learning. The most successful trainers develop a site-specific curriculum that pertains directly to the individual facility, delivering information that not only educates but motivates learners to change behaviours. Good teachers should provide a variety of delivery methods, based on different learning styles, i.e. good graphics for visual learners, clear documentation for those who learn best by reading, demonstration models or actual equipment for hands-on learners, all designed to increase the probability that there will be measurable positive results. Some trainers are even able to integrate their programmes with customer Learning Management Systems, so companies can ensure thorough and convenient training for all employees – at all levels – across multiple sites. Customers can make effective use of their LMS by centralising conveyor training, delivering consistent, high-quality content inexpensively that is available 24/7 and ensuring that all workers have the same
level of education on vital bulk handling systems. This also gives trainers an opportunity to review data that helps identify trends or indicates a need for additional content or refresher courses.
Payback
Expert trainers focus on operational issues and safety, not selling products.
It is estimated that indirect costs of an accident are 5 to 50 times greater than direct costs.
Some conveyor training providers offer online options that are available 24/7. 40
While most maintenance workers are skilled technicians, they are often not expected to understand the conveyor holistically. Conveyors are complex, integrated systems; a change to one component will often have unintended consequences for others, affecting the rest of the system. Without a complete understanding of how conveyors are designed and the components are selected, maintenance becomes an exercise in finding the longest-lasting ‘band aids’ to treat the symptoms rather than solving the root causes. Before long, an accumulation of bad choices in treating symptoms results in a system that cannot operate at maximum efficiency. Some companies continuously focus on an effective training culture (and thereby improve safety) from the top down. Organisations that embrace this approach show significant performance advantages over the competition. The proof is reflected in safety, productivity, and environmental records, along with above industry average financial returns and share prices. While the goal of many training efforts is to maximise productivity, a key element in achieving this objective is improving safety, minimising injuries and the associated repercussions. Literature and research offer many pieces of the puzzle on how safety pays, showing a correlation between reduced expenses and a clean, efficient conveyor. Numerous case studies revealing the positive relationships between safety and productivity are backed up by organisations that gather global statistics on accidents and incidents. Insufficient safety training can be incredibly costly to a plant, with both direct and indirect costs attached to every accident. When plants ensure workers have sufficient training on particular risks, the risks and costs are minimised. Indirect costs are harder to understand, and often the return on investment is unclear to personnel at the plant level. Expert training helps bridge that gap, and instead of simply teaching workers how to maintain a conveyor system, educators must also help students understand the consequences of not performing adequate maintenance. The most effective approach to training examines a plant’s specific conveyor challenges and helps companies run cleaner, safer, and more productive operations by treating the root causes of its problems. When workers and management understand why certain actions are important, as well as the cascading effects that result from poorly trained staff, they are more likely to adjust behaviours and reap the benefits. World Cement BMHR 2022
Conveying news round-up World Cement presents a collection of recent news and technology updates from the conveying sector. Contributions come from: Brelko Conveyor Products, Doppelmayr Transport Technology, & ScrapeTec.
Brelko Conveyor Products: preventing injuries caused by pulley pinch or nip point hazards
Conveyor belt pulley pinch or nip points present a unique set of hazards, which pose potentially fatal consequences. Nip or pinch points exist wherever a conveyor belt meets a pulley. Couple this fact with a momentary lack of focus and this potential can become reality in an instant. Everyone working around these systems has been trained for hours on worker safety, yet accidents still happen.
When installed correctly, traditional guarding cages create a barrier that protects workers from these pulleys. However, this single line of defence has its flaws. Cages must be removed to access equipment for necessary maintenance. When this happens and when the belt is running intentionally, or accidentally starts up, there is nothing protecting workers from hazards. A second, redundant safety device should be installed at each nip or pinch point to protect workers from pulley hazards at all times.
Brelko Conveyor Products has designed, manufactured, and tested such a product: the Nip Guard. This product was designed to prevent injuries caused by pulley pinch or nip point hazards. When properly installed, the Nip Guard stops anyone working around conveyor belt pulley pinch or nip points from being pulled in. Brelko designed and manufactured the product in response to its own service technicians, customers, and industry safety concerns around the hazards presented by conveyor belt pulleys. Conveyor pulleys are
41
The Brelko Nip Guard was designed to prevent injuries caused by pulley pinch or nip point hazards. Image courtesy of Brelko Conveyor Products.
so powerful that they can instantly pull a person in between the pulley and conveyor belt, which can lead to serious injury or death. Placing a Brelko Nip Guard at such nip or pinch points provides workers with protection from pulley hazards. "The Brelko Nip Guard not only protects workers, but it also provides financial risk protection," states Jacques Du Randt, Brelko Africa Service Manager. When the Nip Guard is properly installed at the tail pulley, it blocks tools or debris from entering the nip point. This debris can damage the belt and pulley. This damage, if unnoticed, can cause latent hazards, as the integrity of the pulley or belt is compromised. Brent Weller, Brelko Inc President, discussed the development of the Nip Guard: “Our service teams walk hundreds of conveyors a year. They frequently reported a need for a specialised product aimed at making these areas safer. After initial discussions, our R&D team clicked into gear. Design, concept approval, and extensive field testing and were followed by eventual patent approval. We are extremely excited to bring this unique product to the US market.” Conveyor belt pulley hazards pose significant health risks to workers and can also pose a financial risk for operators. Installing a Nip Guard at all pulley nip or pinch points ensures worker safety and protection from financial loss. The Nip Guard is easy to install, requires little maintenance, adjusts to the belts profile, operates in all conditions and most belt sizes, and is built to be robust for maximum life.
Doppelmayr Transport Technology: quarry restoration solution
The RopeCon system is a combination of ropeway and conventional conveying technology. Image courtesy of Doppelmayr Transport Technology.
After installation of AirScrape, TailScrape and SureSupport the dust emissions were reduced to 0%. Image courtesy of ScrapeTec. 42
Bardon Hill Quarry near Leicester is one of the United Kingdom’s oldest continuously operated quarries. Aggregate Industries UK Ltd has developed a new quarry extension at this strategically important site. In order to sustain quarrying activities, a separate material handling system is required to extract, process and transport overburden for emplacement within the existing quarry as part of its restoration. Doppelmayr Transport Technology has worked closely with Aggregate Industries UK Ltd to develop a unique solution that significantly reduces CO2 emissions and environmental impact when compared with road haulage or the footprint associated with a conventional surface conveyor system. The RopeCon® system is a combination of ropeway technology and conventional conveying technology. Track ropes span 850 m across the entire pit upon which the belt that transports the overburden travels. The RopeCon system includes a reversable second belt that enables simultaneous conveying and World Cement BMHR 2022
NIP GUARD
Summary The Nip Guard is the newest patented product available on Brelko’s extensive line of conveying equipment, offering a unquie saftey screen at all head, tail, & drive pulleys. The Guard is placed just before the nip point of the conveyor, sheilding workers and materials from exposure to pinch hazards, and preventing both injury and equipment failure.
303-544-0817 sales@brelko.us
www.brelko.com/product/brelko-nip-guard-saftey-device/
emplacement activities. During the life of the operation, the RopeCon track ropes will be periodically retensioned to allow the system to be lifted above the placed material. This ability to control the drop height minimises the impact from noise and dust during the operation of the system. This is the first such installation in the UK and transports up to 1000 t of overburden per operating hour. Technical details: ff Section 1 »» Length – 469/500 m »» Difference in elevation – -148/-68 m »» Conveying capacity – 1000 tph »» Speed – 3.3 m/s »» Motor rating continuous – -380/-150 kW ff Section 2 »» Length – 100 m »» Difference in elevation – 0/11 m »» Conveying capacity – 1000 tph »» Speed – 2.6 m/s »» Motor rating continuous – 5/50 kW
ScrapeTec: combatting dust emissions, material spillage, and belt damage.
A cement producer based in the Port of Brisbane urgently needed to deal with a number of issues including: excessive dust emissions, posing major OHS issues; material spillage; belt support and belt sag issues; and minimising production shutdowns. The cement producer's core business focuses primarily on unloading key cement materials utilised for cement production. The finished cement products are then packed into 20 kg bags, and bulk raw materials are also loaded into trucks to service building, construction, and road development projects. A comprehensive site inspection was conducted by ScrapeTec’s Area Technical Representative; it was noted that standard chute sealing was used together with a basic clamping system positioned outside the chute. The current skirting system in place, which had a lack of inner skirting, was insufficient and failed to contain excessive dust emissions and material spillage experienced at the transfer point. Dust and spillage levels were high and constant during the ship unloading process. This provided zero visibility of the 70 m long conveyor tunnel and had greatly affected the maintenance team’s ability to monitor efficiencies and bottlenecks in the production process. Site management was mindful that material spillage was eroding the operator’s bottom line, incurring additional cleaning costs to remove spillage piles and prevent any tripping/slipping hazards. Dust extraction 44
trucks were also necessary to clean the walkway and the tunnel on a regular basis. Dust poses a serious OHS hazard to workers, the environment, and nearby communities. Suppressing dust emissions was therefore high on the agenda and required rectification to minimise any production downtime and improve site availability. Upgrading the transfer point ScrapeTec implemented its AirScrape® application on-site, achieving: a problem free transfer point, with dust emissions and material spillage reduced by 98%; no belt damage, where no future adjustments and maintenance is necessary; exceeding product performance expectations; and more upgrade opportunities in other transfer points. The operator was first introduced to the AirScrape application in 2020 when it was installed on a trial basis. ScrapeTec’s Technical Area Representative touched base with the operator on a regular basis to monitor the AirScrape installation and performance when it was initially trialled in the ship’s unloading transfer chute. Extremely satisfied with the outcomes achieved at this transfer point, the operator welcomed the implementation of The Essential AIR Seal – Dust Containment Combination – as part of ScrapeTec’s phase 2 recommendations. This entailed a few necessary adjustments before the installation of AirScrape, TailScrape®, and ceramic ST-Containment Seal and were fully operational within the chute area. To ensure maximum performance of AirScrape, SureSupport Belt Support System, a vital component of the overall solution was installed in order to avoid the issues of belt sag between the impact rollers. A smooth straight and flat belt surface kept the AirScrape lamellas continuously in the right position with no physical belt contact. TailScrape worked synergistically with AirScrape and provided sealing at the rear, and the ST-Containment Seal delivered on its promise as the first line of against dust and spillage. Prior to the phase 2 recommended installation, there was extremely poor visibility of the tail end of conveyor from the head chute. Yet after implementing the phase 2 recommendations, the maintenance teams were thrilled to report dust and spillage were back under control, and visibility along the 70 m long conveyor is now vastly improved. “The Essential AIR Seal, Dust Containment Solution is a huge improvement in comparison to our initial setup, no belt damage and no ongoing maintenance is required,” reported the Site Manager. The operator has cemented its plans to upgrade all the chutes in the conveyor stream from ship unloading to the stockpiles, representing five transfer points in total. The cement producer now proposes to utilise AirScrape on other applications on-site, this is a positive sign that the issues of belt damage and material loss will be a thing of the past. World Cement BMHR 2022
IDENTIFYING THE WEAK LINK John King Group reviews a case study detailing an elevator chain installation and the subsequent attempts to ensure optimal operation.
A
key consideration for any cement producer when purchasing equipment is confidence that the supplier has a full understanding of not only the product supplied, in this case elevator chains and sprockets, but the practical application of that product as well. Take, for example, supply of bucket elevator chains by John King Chains (JKC) to a principal Indonesian cement producer. With JKC’s industry experience they were confident that the chain, a special series of steel bush elevator chains, was produced with the most appropriate materials and heat treatment specifications that conformed with the customer’s requirements. Despite this high level of confidence, defects in the chains – notably damaged bushes – were reported by the plant in the months following the installation.
As the quality of the chains was recognised to be equal to or better than the previous units supplied, this prompted JKC quality and technical functions to start a review of all aspects of the installation, including chain capacity, selection, and the general design of the double strand centrifugal discharge elevator with chains and buckets independent of each other but driven by a common head shaft The chain was supplied in September 2018. Initial defects were identified on 21 February 2020. A visual inspection was carried out on 23 April 2020 and identified 38 damaged bushes. This was communicated to JKC on 5 August 2020. Of the 38 damaged bushes, 24 pieces were in chain strand 1 and 14 pieces in chain strand 2. It was reported on 9 September 2020 that 4 more damaged bushes had been identified. The occurrence of bush damage was intermittent suggesting this was likely to be the consequence of operational variations.
47
The report noted that the damaged bushes appeared in both strands but predominantly chain strand 1. It was also noted there were 1280 bushes in the full assembly, which were all produced to the exact same specifications. In total there were 42 bushes reported as damaged which comprised 3% of the total number. It was noted that all bushes were heat-treated and carburised in batches and so could be verified as being equivalent. It could be concluded that any non-conformity resulting from the production process would have been a general defect with a far greater occurrence. An independent metallurgical investigation by Element Materials Technology reported the following: ff The bush material conformed to the specification and surface hardness and depth were within the specified limits, appropriate for withstanding hard wearing conditions. ff The material was of a satisfactory standard and can be ruled out as the cause of failure. ff The evidence of witness marks/beach marks were in a transverse direction and showed initiation directionality indicative of lateral stresses. After verifying the suitability of the product and its conformity to the specification, JKC committed to establishing the root cause of the issues, and continued to provide full technical support to the customer.
Design considerations
A full assessment of system design was offered by JKC. The general design follows that of standard mill duty centrifugal discharge elevators although these were generally designed and constructed with one strand of central chain not two. In this case, the original OEM design incorporated two strands of 1500 kN steel bush chain with forged side plates and dismountable bucket attachments. It was later revealed that the OEM chain had experienced link plate failure after a period of operation which was likely to have been associated with on/off overload and or impact during operation. Although some questions remained outstanding JKC commenced a review of the chain capacity, selection, and general design of the centrifugal discharge elevator. According to the OEM technical description, the elevator was a double central chain bucket elevator machine type 1600 x 48100 referring to bucket width of 1600 mm and chain centres at 48.10 m. The material to be transported was limestone with a bulk density of 1.6 t/m3 with a particle size of 0 – 100 mm. Maximum temperature is 100˚C, with a design capacity at 900 tph (563 m3/h). A full review of the design capacity was conducted based on twin strand operation (combined capacity) and individual strand operation (single strand capacity). The conclusions reached were clear. Combined capacity marginally exceeded requirements at 570.24 m3/h and/or 912.38 tph. Single strand capacity was reported as 285.12 m3/h and/or 456.19 tph. The results indicated that the elevator could deliver the design capacity of 900 tph, but this was reliant on both chains being loaded equally to 65% of bucket fill. It could be proven beyond doubt that when considering the design of the elevator, this was not happening.
Observations gained from site survey Figure 1. Illustration of material and conveyor interaction.
Figure 2. Chain Knuckling on head wheel as a result of inconsistent tension. 48
John King site service engineers visited the customer to gain an understanding as to what was happening during operation. The subsequent report listed a number of potential problem areas and production inefficiencies. These included, but were not limited to the following: ff The infeed into the side of the elevator as opposed to a split chute with delivery directly into the buckets will undermine the performance of the elevator to a considerable degree and cause spillage and flooding in the boot. ff The inlet chute into the elevator in this case should allow a minimum of three
World Cement BMHR 2022
buckets between the tail shaft and inlet. It was concluded the distance was inadequate. ff The infeed into the side of the elevator will cause a pendulum action which will create side load. ff Correct tensioning of this type of system is crucial since adequate tractive force between chain and drive wheel is essential. It was considered that the tensioning was inadequate. ff The design review concluded that the combined design capacity can be achieved if the buckets are 65% full. The JKC engineer stated with certainty this would not be happening. The design capacity of one strand is at its limit and does not allow for any excess material. The reality is that the total infeed will be delivered to one strand.
EXPERIENCE THAT TOWERS ABOVE THE REST
It was the conclusion of the JKC assessors that the root cause of the issue with the chain was the position of the infeed. This has an impact on the operation of the elevator chain with resultant damage to components. This is corroborated by the comments made in the metallurgical report from Element Materials Technology.
Consequences of observations
Flooding of the boot will occasionally occur and if this is continual, it will impact on the satisfactory operation of the elevator and undermine the service life of the running gear (chains and wheels). As stated, the bulk delivery is to one strand with the undoubted consequence of overload, spillage, and flooding in the boot of the elevator. Flooding of the boot will cause variations in tension with intermittent knuckling of the chain as illustrated in Figure 2. Thereafter, as the chain bush re-engages with the traction wheel rim, heavy impact can occur which will damage the case of the bush. This is clearly what was evidenced in the intermittent chain bush damage. Once the case is damaged the expected outcome is that the wear will accelerate and this is only accentuated by larger and heavier chains as in this case. Flooding of the boot can reach a point where the system is jammed with excessive power at the head wheel allowing the traction wheel to turn under the chain. In these circumstances, the bushes in contact with the wheel will be damaged. Spikes in absorbed power should be detected with trip limit warnings if set correctly. As stated, to deliver material to one side of the elevator on a centrifugal discharge system and not directly into the buckets will cause continual flooding in the boot and negatively impact the chains. One element is the pendulum effect,
™?
Why Choose
z Experience - More than 35 years of tackling the most difficult silo cleanout projects in 30+ countries worldwide z Safety - Professional service technicians are MSHA and OSHAcertified and adhere to a rigorous continuing education program z Capability - We conquer the most difficult cleanout projects in the world with our proprietary silo cleaning technology
www.molemaster.com 740.374.6726 800.322.6653 (USA) 06/22 02254
which will cause the chain to sway. Chains of this construction are not able to manage the side load which occurs as a result of chain sway. This lateral movement was identified in Element Materials’ report where high magnification revealed regions of cracking in a transverse direction and in another instance where witness and beach marks were found in a transverse direction, indicative of lateral stresses caused by this condition.
Although the internal gravity take-up unit (IGTU) is the most effective means of tensioning elevator chains of this type, continual and extreme flooding in the elevator boot will undermine its effectiveness. JKC recommended the use of sprockets in place of plain rimmed traction wheels because as the material packs within the plain bearings of the unit, the positive engagement of the sprocket tooth on the bush will force the shaft to rotate. In extreme cases, however, the bearings will be subject to seizure and the IGTU will likely be forced up the guide chain introducing slack into the system with the consequences highlighted in Figure 2. Friction drives, as in this case, can be more forgiving than sprockets because during operation it is the diameter that is lost and the negative impact of worn sprocket teeth can be avoided. Successful operation however is dependent on adequate tractive force between chain and drive wheel. Where the weight of chain, buckets, and material are inadequate, the bearing pressures may not be enough to create positive traction. In addition, where the elevator’s operational parameters are unable to keep the elevator boot clear, build-up of material and dredging can have the same effect. Inadequate tension can also create Figure 3. King series JKB2100/A/180/K24x2 after 18 months slippage at start-up which is often in operation. The condition, including damages to bushes, was the cause of accelerated bush excellent. wear/flatting. Start up under load is an extreme version of this. This article has already referred to the issue of tension weights and it was clear at the outset, and as highlighted in the original report, that this was inadequate in the plant’s initial implementation. The continuance of swaying is primarily the consequence of side loading, but could be reduced with the application of tension. This should be considered in a more systematic manner. For IGTUs of a conventional design, an approximate counterweight mass of 1500 kg per chain will apply. This includes the take-up frame assembly with shaft, return sprocket, bearings, and weight box. This provides a good starting point and can be incrementally increased as required. The bush’s outside diameter and chain link pitch hole are CNC Figure 4. Difference between standard bucket option and JKHP machined to close tolerances. standard as D-9515-20.
50
World Cement BMHR 2022
This ensures consistent and high interference fits. Heavy impact (highlighted in Figure 2) can also undermine the integrity of the interference fit and in extreme cases allow the bush to turn, as was also identified in the Elements Materials report. Flooding of the boot section of the elevator with variations in tension will cause slippage of the chain bush on the traction rim. This can lead to extreme friction with burning/overheating as was noted in the Elements report. The temperatures reached in these conditions (exceeding as little as 200˚C) will normalise the surface carburising and undermine the hardened case leading to accelerated wear and flatting as experienced. Flooding of the boot section of the elevator where larger particle sizes are handled (up to 100 mm) can be additionally detrimental to the chain. Larger lumps will become trapped as the chain opens and closes as it traverses the tail sprocket as illustrated in Figure 1. This clamping action will again cause slippage on the traction wheel and in extreme cases create cyclic fatigue of chain link plates leading to catastrophic link plate failure. One solution to increasing capacity can be achieved with JKHP (high capacity) buckets as shown in Figure 4. In this case the chain is installed with the platform inboard and ‘wrap around’ buckets are employed to increase throughput and reduce spillage, thus helping to achieve a marked reduction in boot flooding.
Premium powder, premium packed From automatic bag filling machine to stretch hooder: our customized packaging solutions make sure your powders maintain their high quality.
Conclusion
It is clear that the design of the elevator is fundamentally flawed. As a direct consequence, the chain supplied, proven to be of the highest integrity, had sustained operational damage. It was advised (after the event) that there had been historical issues with chain performance as a consequence of design shortcomings. In light of this it is clear that JKC was not given the full history and if fully informed, the company’s experience in the design and operation of mill duty centrifugal discharge elevators would have been available to eliminate the historical issues in the elevator and establish operational reliability and extended service life. The most important element of the elevator is the ‘running gear’ comprising the chain and wheels so it is perfectly logical that cement mills should engage companies that have all-round experience, not only in the production of high quality running gear, but also a full understanding of the application. It is also important to work with suppliers who will stand by their customer and overcome shared challenges as part of a process of continual improvement.
Finally: a 100% waterproof packaging Thanks to the AROVAC® technology you can opt for bags that are 100% waterproof and completely sealed. This offers you maximum protection and carefree transportation of your product, even when stored outside for longer periods.
Aino Saarelainen and Panu Kantosalo, Cross Wrap Oy., discuss how increasing freight costs affect the use of alternative fuels in the cement industry and assess ways in which these costs can be best minimised.
52
Efficiency is key: transporting and storing alternative fuels
T
he transportation industry is facing historical uncertainty and price increases. Freight expenses are skyrocketing due to high demand, increasing fuel costs, and a driver shortage in Europe. This phenomenon affects many industries, including cement manufacturing companies who need to transport alternative fuels to their plants. Alternative, waste-based fuels are considered by many to be
a suitable substitution for fossil fuels in cement manufacturing. However, transporting and storing these alternative fuels is not always straight-forward. To combat the rising costs and uncertainty, the fuels need to be transported, handled, and stored as efficiently as possible. Finland’s Cross Wrap Oy has operated in the waste-to-energy sector for nearly three decades. The company’s expertise in the field has led it to develop
multiple solutions for the industry, many of which have been applied to cement manufacturing. These solutions can address various problems in alternative fuel handling, transportation, and storage.
RDF and SRF: a more sustainable option
Alternative fuels such as RDF and SRF have long been potential alternatives to using coal, natural gas, and oil in
53
cement kilns. Waste-based fuels are an ideal option for cement kilns in terms of sustainability – high-temperature kilns destroy waste material in an energy-efficient and environmentally friendly way. The impact of fuels in the cement manufacturing process is relatively high, as 40% of total emissions of cement manufacturing can be attributed to the fuel. Switching energy sources from fossil fuels to alternative fuels can currently offer an economic incentive, as oil and natural gas are becoming more expensive. This is partly due to the inflation, and economic sanctions imposed upon Russia following the country’s invasion of Ukraine. There is a lot of talk about the green transition, as the steep price increase of fossil fuels has incentivised many countries and industries to opt for more sustainable energy sources. Fuel consisting of recovered waste is one of the
preferred options. Could this be the case for the cement industry as well?
Sky-high freight costs
Why is transportation so expensive at the moment? There are many factors that have impacted rising costs. Price volatility and freight delays have affected many industries, including alternative fuels and any industries using them. Europe is suffering from truck driver shortages in land freight due to Brexit, new EU restrictions, and an ageing work force. Combining the lack of drivers with rising oil and fuel costs, freight is becoming increasingly expensive. Moreover, the effects of COVID-19 are still lingering: production and consumption have again begun to rise, increasing the demand for freight and transportation. However, the supply has not been able to meet demand, which increases transportation pricing. Due to the steep costs and unexpected delays in transportation, cement manufacturers burning alternative fuels in their kilns need to be prepared. Efficient material handling methods are more important than ever and stabilising and maintaining a buffer storage of fuel and transporting it in a cost-effective way is a The costs of transportation are steadily rising due to multiple factors in the necessity. freight industry and global economy.
Baled and wrapped waste in transportation
Wrapped square RDF and SRF bales save space and costs in transportation. 54
Many cement kilns purchase alternative fuels from waste-to-energy manufacturers, who can sometimes be located far away from the actual cement plant. Baling and wrapping waste-based fuels is the best way to ensure easy and effortless handling and transportation. Baling helps to condense the World Cement BMHR 2022
t RWM Meet us a th le Live 14 Letsrecyc and 15th ber. of Septem . 90 stand R-P
THE WORLD´S SMARTEST
BALE OPENERS AND DEWIRING MACHINES Automatic Cross Wrap Bale Openers and Dewiring machines cut, remove and coil wrapping film and wires from the bale.
CROSSWRAP.COM | SALES@CROSSWRAP.COM
An Industrial IoT Solution for ModernLogistics from Axians IAS More efficient logistics processes through digitization and efficiency optimization Sustainable load planning and dispatch automation – contactless, paperless, secure Consultancy, development, implementation, and support Software + hardware + professional services Ready to start saving time and money with VAS?
Axians Industrial Applications & Services GmbH Hoervelsinger Weg 17 · 89081 Ulm · Germany info@axians-ias.com · www.axians-ias.com
ROAD2 YARDr & 2 Oct 25, 20
Webina to Retn it’s Time e h W : s c ti Logis dmap Digital Roa r u o y k in h (London), York), 2pm 9am (New /Rome) 3pm (Berlin
waste material into a dense bale, which allows each bale to contain more fuel material. Dense bales are more cost-efficient in freight, as more fuel can be loaded into one truck or shipping container. Compared to loose waste material, baled RDF and SRF save much more space, during both transportation and storage. Moreover, wrapping the bales gives additional benefits to transportation and handling. Loose or unwrapped alternative fuel material is difficult and messy to handle. Wrapped bales do not litter, leak, cause unpleasant odours, attract pests, or lose their shape. Cross Wrap is an expert in wrapping messy materials like alternative fuels. The CW 2200 Bale Wrapper and the CW Direct Bale Wrapper, the company’s flagship products for the waste industry, automatically wrap waste bales on all sides, creating a neat bale that is easy to handle. These wrappers can easily be
modified to suit the needs of different plants and production capacities, and the automatic wrapping can be optimised to fit different handling and transportation requirements.
Why opt for square RDF or SRF bales?
In the baling and wrapping industry, the question remains: whether to opt for square or round bales? The form of the bale has an actual effect on its operational efficiency. Square, or cubical, bales are the best choice for many operators who require high density in their material. These operators often include the manufacturers of waste-based fuels. Naturally, a denser bale means more fuel material can be fitted into a cubic meter. Waste material is suitable for high pressures, as the material is not damaged in baling. The square bale shape is also stronger bale, which increases the ease of material handling. Compared to square bales, round bales are less dense and softer in the middle of the bale. Where square bales can hold up to 700 – 1000 kg/m3 of material, round bales usually average 500 – 700 kg/m3 of material. In a time where freight costs are through the roof, denser bales ensure that every shipping container or truck journey is as cost-effective as possible. More material Cross Wrap solutions can solve various problems in alternative fuel shipped in one batch handling, transportation, and storage for the cement industry. means more ‘bang for the buck’.
Efficient storage helps to create a buffer for potential fuel shortages
Cross Wrap bale wrapping helps to create dense bales and is an economical way to wrap waste fuel materials. 56
The current global geopolitical and economic turbulence has had multiple ripple effects. Inflation increases pricing, waste recovery numbers are falling, and logistics are becoming increasingly expensive due to rising fuel costs. World Cement BMHR 2022
YOUR CONVEYOR SPECIALIST
Design & Manufacturing: • Belt Conveyors • Belt Elevators
Own engineering Project development Preassembled delivery Services: • Technical Assistance • Installation • Commissioning • Spare parts Ctra. N-232 Km.252a Utebo, Zaragoza (Spain)
•
Tel. +34 976 770 656
•
www.cintasa.com
Layout.indd 1
27/03/2018 08:41
Engineered for handling everything from the finest powders to the most abrasive agregates
Heavy Duty Slide Gates
IN YOUR WORLD There’s no time for down time.
Diverter Valves
That's why we make solids & bulk handling components that are made to perform.
Learn more about Vortex Slide Gates, Diverters, Iris Valves & Loading Solutions at:
www.vortexglobal.com Aerated Conveying
Loading Spouts
This combination of events has also led to rising costs of waste-based fuels and made them more scarce. Many operators who utilise waste-based fuels in their business are aiming to increase their RDF or SRF stock in order to avoid trouble in production. In a situation like this, efficient storage methods are key to maintaining the energy efficiency of the fuel. As suggested before, square bales are an optimal solution for storage. Due to the dense nature of the bales, they have a smaller footprint, taking up less space in storage. They can also be piled into higher stacks, up to stacks as high as ten bales, without safety risks or problems with the bales losing their form. Wrapped RDF or SRF bales do not even require large storage spaces, as they can be safely and efficiently stored outside. Waste-based fuels have a small risk of fire due to the gases which form within the waste. Square, wrapped waste bales pose a smaller fire hazard, as the bales can be stacked closely together with smaller air gaps between the bales. Maintaining the calorific value of RDF and SRF is largely tied to wrapping the material. In addition to the benefits mentioned above, the plastic film protecting bales creates a protective barrier to the waste material. Fermentation processes can also easily begin in waste-based fuels. This diminishes the calorific value of the fuel, making the fuel less energy-efficient in incineration; in addition to preventing fermentation, the plastic film also protects the material from weather conditions, which could damage the material.
Opening bales at the end of the line
The end of the logistics line for RDF and SRF bales in the cement industry is the kiln. When the waste fuel is baled and wrapped, it must also be opened and loosened again for it to be fed into the cement kiln. Cross Wrap’s CW 3600 Bale Opener is designed for opening RDF and SRF bales. The machine opens the metal bale wires and plastic wrapping, removing them from the fuel material infeed. This ensures that the alternative fuel that ends up in the kiln is as high quality as possible. Moreover, removed bale wires and plastic can be further recycled. An automatic solution for opening the bales decreases the need for potentially dangerous manual labour.
Ensuring smooth alternative fuel handling
It is unclear when or how the ongoing turbulence in fuel prices and freight costs will subside. Investing in machinery that can ensure a steady fuel source for a cement kiln is an option to be considered. The years of experience in working with alternative fuels, cement manufacturers and the waste industry has helped Cross Wrap to hone the company’s offering to the field. As mentioned above, Cross Wrap provides multiple solutions for efficient alternative fuel handling in all stages of the supply chain. Cement manufacturers around the world rely on Cross Wrap Bale Wrappers and Bale Openers to ensure their alternative fuel handling is smooth and efficient with machinery that provides competitive advantages in labour, storage costs, and safety.
About the authors
Aino Saarelainen (MSc.BA) is a recent addition to Cross Wrap’s marketing team. She is a graduate from Aalto University School of Business and has worked at Cross Wrap for ten months. In her role as Content Creator, she combines her interests and expertise in writing and learning more about the waste recycling industry, the circular economy, and sustainable development.
The CW 3600 Bale Opener removes bale wrapping and wires from the alternative fuel infeed. 58
Panu Kantosalo (M.A. & B.A.) has been Cross Wrap Oy´s Marketing Manager for the last four years. His work consists of gathering the latest information on waste-to-energy, circular Economy, packaging, and logistical solutions, and converting them into an understandable form, and whose interest in the circular economy and sustainability keeps him studying and working hard for a more sustainable world. World Cement BMHR 2022
Sigrid Eder-Ince, Starlinger & Co., explains how optimising cement packaging will be a major factor in curbing the industry’s greenhouse gas emissions.
A
round 4.1% of global CO2 emissions are caused by the cement industry.1 While process emissions from clinker production cover the biggest share, thermal emissions as well as indirect emissions – such as from electricity production, for example – also contribute significantly to the greenhouse gas emissions produced during cement manufacture.
Savings potential for greenhouse gases
Strong, tear-proof cement packaging can help to reduce emission output by preventing tons of cement from going to waste due to sack breakages. By reducing breakage rates, cement losses can be cut significantly, and so can the quantities of new cement produced to replace the lost quantities. Made of woven polypropylene tape fabric, AD*STAR block bottom valve sacks,
59
developed by Starlinger & Co GmbH, are highly resistant to breakages.2 They are made from coated polypropylene tape fabric and sealed with a patented hot-air method. The use of high-strength polypropylene tapes for fabric production and the tight sealing of the sack bottom and top ensure low sack breakage rates even during rough handling, dropping, or after contact with water. A Life Cycle Assessment commissioned by Starlinger in 2016 showed that AD*STAR sacks have a lower global warming potential (or carbon footprint) than paper sacks. 3 A key factor behind the positive results of AD*STAR sacks in this study are their low breakage rates over the course of their life cycle: They remain at 1% during the entire usage phase of the sacks – i.e. from filling, transport, and storage until the unpacking of the cement – compared to 4 – 5% in the case of paper sacks. This means that if AD*STAR sacks are used, less cement is lost and needs to be replaced, and less packaging is needed – consequently, less greenhouse gases are produced.
Millions of tons of CO2 emitted due to extra cement production could be saved each year.
Sustainability in the bag
Reduced raw material input, 100% recyclability, and inclusion of recycled content are the main steps that need to be taken to realise greater sustainability in cement packaging. AD*STAR sacks are designed for recycling: They are a mono-material packaging solution, made of polypropylene and produced without the use of glue or sewing threads, making them easy to recycle. The main challenge remaining when it comes to recycling these sacks, is the removal of residual cement dust, and establishing collection systems for the sacks to create a closed packaging loop, which would be the ideal goal. Currently, most of these sacks worldwide are entering a second life cycle after their use as cement packaging, e.g. as packaging for other materials, carrier bags, or even as simple roof coverings, whereas paper sacks are usually incinerated after usage. Regarding recycled content, recycled polypropylene produced mostly from other packaging applications is already used for AD*STAR sack production. Starlinger has been working on developing the technology to recycle post-industrial polypropylene packaging and has achieved positive results. Because polypropylene degrades during the recycling process, it is important to ensure that the recyclate has a very high quality. Otherwise it cannot be used in tape extrusion and weaving, and sacks with recycled content will not have the same strength like sacks made from virgin AD*STAR sacks are available in many sizes and with material. Scientific trials carried out additional features such as the easy open closure. by Starlinger showed that a recycled content of 50% is possible without negatively affecting the standard properties of an AD*STAR sack, given the recycled material quality fulfils the prescribed quality standards. Resource efficiency is a major focus for Starlinger’s technology development whilst also aiming for the highest quality and efficiency in packaging production. Starlinger machines are energy-efficient, easy to handle, and operate with minimum raw material input and low waste generation. AD*STAR sack production machinery has been designed to manufacture sacks in an Minimal size variations make AD*STAR sacks well-suited efficient, energy-saving production for automated filling lines. process – from tape extrusion, 60
World Cement BMHR 2022
stretching and winding, to weaving, laminating and conversion. The use of stretched polypropylene tapes is the reason why the sack weight of an AD*STAR sack designed to carry 50 kg can be as low as 62 g, while a 2-layer paper sack of the same size weighs about 140 g, with a PE film sack weighing as much as 150 g.
The technology
Starlinger provides the full range of technical equipment together with the know-how needed for the production of AD*STAR sacks: polypropylene tape extrusion lines, tape winders, circular looms for fabric production, coating and printing machinery, as well as the ad*starKON block bottom sack conversion lines. The entire range of this technology has been developed with a focus on high sack quality and resource-conserving production. This ensures the high strength and durability of the sacks, as well as smooth and trouble-free cement filling on the most modern filling lines. Starlinger’s AD*STAR conversion lines cover a broad format range – from a sack capacity of only 5 l up to 115 l. Currently, the company is developing a technology to increase the coefficient of friction (COF) of AD*STAR sacks to ensure stable stacking. An anti-slip surface makes storage and handling of cement sacks even safer, especially in humid or dusty environments.
Currently, around 25 billion AD*STAR sacks are produced worldwide on Starlinger machinery every year. The strengths of these sacks include the following: ff High strength and durability – reducing CO2 emissions due to low breakage rates. ff Raw material savings due to the low packaging weight. ff Easy-to-recycle mono-material packaging solution. ff Suitable for automated filling, handling and palletising. ff Fully automated sack production. ff No spillage or leaking because of the polypropylene coating. ff Adjustable coefficient of friction (COF) – ad*grip technology. ff Adjustable air permeability due to optional micro-perforation – keeps dust formation to a minimum and protects moisture from entering the sack (longer shelf life). ff Tamper and theft-proof. ff Attractive sack design with high-quality print or laminated BOPP film for improved brand promotion.
Conclusion
The need to reduce the carbon footprint of the cement industry has led to increased efforts to curb greenhouse gas emissions in all areas. When it comes to cement packaging, AD*STAR block bottom valve sacks offer a sustainable alternative. They are made of coated polypropylene tape fabric, making them a very strong and durable packaging for cement. With a breakage rate of around 1% over the course of their life cycle they are clearly more reliable than paper bags, which have a breakage rate of between 4 – 5%. By using AD*STAR sacks, the amount of cement lost due to spillage is significantly reduced. Tons of cement required to replace losses no longer needs to be produced, and CO2 emissions are thus reduced.
References
In many countries, AD*STAR sacks are reused multiple times due to their durability. 62
1. OLIVIER, J., PETERS, J., ‘Trends in Global CO2 and Total Greenhouse Gas Emissions: 2019 Report’ – PBL Netherlands Environmental Assessment Agency; IES of the European Commission’s Joint Research Centre, 2020, p. 20. 2. AD*STAR is a registered trademark. AD*STAR sacks are exclusively produced on Starlinger machinery. 3. DAXNER, T., KOSIŃKA, I., and MERL, A., ‘Carbon Footprint and LCA of AD*STAR Technology’, Leinfelden-Echterdingen: PE International AG (later thinkstep AG, now part of Chicago-based Sphera Solutions, Inc.). 2016. World Cement BMHR 2022
T
he cement industry is growing every year due to the continued expansion of industrialised and urbanised areas and the construction of new buildings, roads, and infrastructure, with much of the demand coming from emerging economies. At the same time, cement factories are major contributors to global CO2 and dust emissions, both of which have a significant environmental impact. Recently, a common goal has been set to keep any future global temperature rise below 2.0˚C, and ideally below 1.5˚C. More than 77 countries have committed to control and reduce the environmental
impact of the cement industry by 2050. Reducing the emissions of the cement industry will play a pivotal role in addressing the climate challenge. Companies will need to identify the best paths toward the 2050 target through operational innovation, eco-friendly equipment, and modern technology. Bedeschi is committed to helping reach this global goal with its 110 years of experience and the wide variety of solutions that it can offer. The company's R&D department works to improve the capability of its systems, focusing on environmental protection, energy efficiency, and investments into eco-friendly and
innovative equipment and pollution prevention. Bedeschi is working to improve its machines to reduce dust emissions and material spillage during bulk material operations through several avenues: a careful selection of belt width and speed according to the handled cargo, the installation of belt conveyors and trippers in enclosed galleries, the use of pipe conveyors and enclosed conveyors, the use of gas cleaning and water spray for dust suppression, telescopic or spiral chutes, implementation of eco-hoppers, and the use of different conveying systems, like screw conveyors and chain conveyors.
TURNING THE CEMENT INDUSTRY GREEN
Fabio Chignoli, Bedeschi, outlines the route that companies operating in the cement industry need to take to ensure the highest environmental standards. 64
Besides avoiding the spillage and dust emissions, the use of a pipe conveyor allows for the removal of several transfer points between straight conveyors. This solution reduces the consumption of energy needed to handle the material, not to mention the energy used for the filters and other suppression systems to lower dust emissions. Fewer transfer points in a plant means fewer chutes, cables, and other auxiliary equipment, with a positive payback in terms of the erection timeline and related environmental cost. Without transfer towers, a lot of steel fabrication is saved as well as foundation works and erection activities, thus reducing
the overall carbon footprint of the plant and its environmental impact. Moreover, Bedeschi is proud to work closely with its clients in projects intended to use alternative fuels to limit the use of fossil-type fuels, as well as reducing plant power consumption. The following examples are some Bedeschi’s latest applications to guarantee environmental safeguarding and avoid dust pollution:
MELON – Chile
Bedeschi supplied Melon S.A. with a new eco-hopper to be operated in the austral port of Punta Arenas, Chile.
The eco-hopper is designed for the direct unloading of clinker to trucks at a rate of 600 tph and is designed to work with 12 m3 grabs. The machine is equipped with pulse-jet bag filters with high filtration capacity and with low compressed air consumption: an economical and flexible solution to satisfy the stringent environmental standards required. “The eco hopper has been a crucial part of the Project, and the results in environmental matters are very satisfactory” confirmed Mr. Pedro Pinto, Corporate Technical Manager of Melon. A set of 4 bag filters are mounted in the space between the upper receiving hopper and the hopper
Bedeschi eco-hopper in Punta Arenas, Chile.
65
main body. The bags are automatically cleaned with a pulse jet system and all the particles removed from the bags simply fall inside the hopper itself. Access platforms are provided for the ergonomic and safe replacement of the bags as well as the addition of a fan outlet, with silencer, for noise reduction. The eco-hopper is equipped with a fully covered feeder conveyor to avoid dust dispersion due to the wind action and it maximises the efficiency of the dedusting filters. For clinker loading inside the truck there is a dust controlled telescoping spout. The automatic lifting control keeps the skirt in contact with the forming pile, to avoid fugitive dust. An aspiration system keeps the inside of the chute depressurised. The Bedeschi eco-hopper is designed to contain and minimise emissions during every unloading phase, both from ship to hopper and from hopper to truck, and as a result, the company “has been able to fulfil and exceed the environmental regulations,” says Mr. Pedro Pinto. “The teamwork between Melon and Bedeschi has developed a creative tailor-made solution that allows it to operate in a multipurpose port,” he added. In fact, the eco-hopper is designed with a special support structure that allows a solid anchoring of the hopper to the pier structures during unloading operations, but at the same time it allows the machine to be moved by means of SPMT when not in use. This configuration is made necessary by the multi-purpose nature of the Punta Arenas port and due to structural limitations of the existing pier. These operational constraints have forced Bedeschi’s engineers to find a winning solution in terms of flexibility of use, weight limitation, and structural strength.
SECIL – Portugal
Incorporating alternative fuels such as waste and biomass to replace fossil fuels, a multi-decade trend in the industry, could reduce emissions by nearly 10% by 2050.
SECIL Group has awarded Bedeschi with a contract for the supply of a new pipe conveyor to handle different kinds of alternative fuels at the Outão cement plant in Portugal. This project further strengthens the cooperation started with SECIL more than twenty years ago and it is part of the major R&D Clean Cement Line (CCL) Project. The CCL project, aims to bring the Outão cement plant to the forefront of energy efficiency and produce the lowest CO2 emissions among European cement producers. The Project is partly funded by the Portugal 2020 Government incentives programme, and it aims to develop a new concept of cement production. Bedeschi’s supply to the SECIL Group will contribute to eliminating dependence on fossil fuels. The concept of Industry 4.0 will become essential for the plant’s management when improving efficiency and optimising processes, therefore a digitalised system will be integrated into the whole plant. Bedeschi’s engagement in this project is part of the company's activities aimed at reaching some of the sustainable development objectives, especially environmental protection, as established in the Agenda 2030 by the United Nations. For many years, Bedeschi has been working hard to achieve these goals. The pipe conveyor with a diameter of 250 mm and conveying length of 350 m will enable safe and clean transportation of alternative fuels at a rate of 300 m3/h. Bedeschi will design and supply the complete pipe conveyor system, delivering the structure in preassembled transportable modules to allow for a smooth and trouble-free erection. The pipe conveyor solution was selected for this application as a modern and environmentally friendly transport system solving numerous problems associated with conventional conveyor systems (i.e. spillage of materials, limitations with regard to steep incline and curve layout, etc.) and the transportation of difficult materials.
Summary
There is not one global solution that fits the needs of every stakeholder in the cement industry, and it will be a long journey to turn it into a green industry. Bedeschi continues to find its own solutions to make a positive impact on this process.
About the author
3D design of Secil pipe conveyor. 66
M. Sc. Eng. Fabio Chignoli works for Bedeschi as Sales Manager for South America, Spain, and Portugal and Key Account for cement industry. He graduated with a degree in Aerospace Engineering at the Polytechnic of Milan, he has more than 15 years of experience in the cement industry with expertise in material handling and air pollution control. World Cement BMHR 2022
Georg Lechner, Head of Sales – Industrial Minerals at Scheuch, answers some questions to mark the 10th anniversary of the semi-dust SCR system and celebrate a decade of exhaust gas cleaning expertise.
Ten years ago, Scheuch commissioned the world’s first semi-dust SCR system. Before we get into the details of this project, can you tell us a bit more about Scheuch? Georg Lechner (GL): For almost 60 years now, Scheuch has been providing innovative air pollution control and environmental technology such as dedusting, conveying, and flue gas cleaning for industrial applications around the world. Its headquarters are located in Aurolzmuenster, Upper Austria. Catering to a wide range of industries including industrial minerals, energy, metal, wood-based panels and glass, to mention a few, Scheuch delivers a complete portfolio for dedusting, pneumatic transport, and exhaust flue gas cleaning systems. The company covers a comprehensive range of turnkey services that encompass sales, project management, design, research and development, manufacturing, assembly, commissioning, and after-sales service.
Scheuch focuses on extensive research and development throughout all of its work, with the aim of elevating its position as a technology leader even further.
What differentiated this new technology from other SCR systems?
GL: The SCR process itself is nothing new – what really made this technology special when it was launched was its adaptation to the cement industry. Upstream cement processes involve high dust concentrations and a specific gas, so the conventional SCR systems that had been used in the past didn’t have technology that was stable enough for continuous operation. The new technology developed by Scheuch represented one of the first large-scale applications of this type in the cement industry worldwide. Today, there is a whole host of process-adapted SCR technologies available for reducing NOx emissions: high-dust SCR, low-dust SCR, and semi-dust SCR with a dry electrostatic precipitator
67
as a pre-separator and integrated gas conditioning tower in the catalytic reactor. A gas conditioning tower integrated in the SCR system then maintains the maximum filter inlet temperature for the downstream emc bag filter after the catalytic reactor. Scheuch had already begun developing and optimising the technology and design of SCR systems years prior to that by testing under similar conditions in pilot systems. From the beginning, the primary goal was to produce a stable configuration that would make it possible to incorporate the new application into the existing process. Alongside this, however, we also had the goal of gathering long-term experience about the service life of catalytic elements, the best and most efficient method of cleaning, separation efficiencies and so on, so that we could see where else the system needed to be improved upon.
Why was Lafarge’s Mannersdorf plant selected as the first location?
GL: SCR technology has been able to establish itself as a conventional exhaust gas cleaning technology in fossil-fired power systems, waste incineration and
other industrial areas, and has been state-of-the-art for several decades now. However, the cement industry didn’t fully adopt it until 2013, mainly because there was so much uncertainty about catalyst stability. Austria and Germany’s political spheres began showing more of a commitment to reducing emissions in the cement industry, and this is where Lafarge came in: as the largest cement plant in Austria, it has always upheld its responsibilities in the area of environmental issues and has also taken on a pioneering role in NOx reduction. Scheuch and Lafarge have worked closely together for a long time. In 2005, Lafarge Mannersdorf was the birthplace of Scheuch’s emc (energy minimising cleaning), the advanced bagfilter cleaning technology – and it then became home to the large-scale pilot project for semi-dust SCR technology, which reinforced the sense of partnership between the two companies. The pilot project also proved to be the perfect venue for reconfiguring the cement system. The kiln line was constructed during the energy crisis of the 1970s and designed with energy optimisation in mind, working with the most advanced technology that was available at that time. This meant low kiln exhaust temperatures in the range of 290˚C to 340˚C. A unique feature of the kiln is a dust content of 180 g/Nm3 – and this is what led to the world’s first industrial SCR semi-dust system for NOx separation being installed, after careful analysis.
Did this installation pose any challenges? If so, how were they overcome? Georg Lechner, Head of Sales Industrial Minerals, Scheuch GmbH.
Regenox system (Märker Zement GmbH, DE). 68
GL: The scale-up from the pilot system to a large, real-life industrial system was a major challenge. This sort of work is all about achieving the correct design and flow behaviour, planning the system down to the finest detail and integrating the SCR unit with the production line. The system was installed in an existing pre-heater tower that was part of the old kiln line, a process that was extremely difficult and demanding due to the limited space available. In many cases, it wasn’t possible to pre-assemble all the system components at the site. One challenge that we managed particularly well was the unusually high crude gas dust content. It was vitally important to analyse the gas and dust distribution in advance and factor in the real conditions present in the large-scale system. Cleaning the catalysts is one of the most important details – not only do the cleaning devices have to be performing well enough to keep the catalyst surfaces active, but they also have to be as soft as possible to prevent mechanical damage. The catalyst in the SCR system has to experience an even flow to make things run as efficiently as possible. World Cement BMHR 2022
th
ANNIVERSARY EXPERT FOR EXHAUST GAS CLEANING
2012 2022
AT H S U C T VISI POWTE 1 4-11 H T BOO
TECHNOLOGY FOR CLEAN AIR
A FULL RANGE OF FLUE GAS CLEANING SYSTEMS Most trusted name in the environmental technology sector
WWW.SCHEUCH.COM
Another major challenge, of course, is commissioning a system with completely new configurations, while keeping the production-related process conditions in mind. A lot of patience and accuracy is required from the commissioning engineers when making the fine adjustments in the continuous operation of the system, with the aim of optimising performance.
What did you learn from this installation?
GL: We learned that our systems are able to maintain stable operation even if the conditions are very difficult. To achieve this, it’s essential to analyse the process conditions in whichever cement system we are working on and adjust the configuration to the operating conditions at that particular customer’s site. The learning curve increases with each new project, so the experiences from pilot projects in the industrial environment naturally flow into other projects and we’ve been able to improve our design principles and simulation models for cement plants as a result. The ability to check, verify, or even adapt the model-based design data using actual operating data increases the quality of our simulations. That knowledge, along with our understanding of the process and innovative
Semi-dust SCR system (Lafarge Zementwerke GmbH, AT).
RTO system, with the option to expand it to include deconox® (W&P Zement GmbH, AT). 70
strength, really helps us show our system customers that we are the right choice. Of course, all this experience also flows into product and technology development, which means we can continuously expand our portfolio.
What other technologies has Scheuch developed? How do they complement SCR systems?
GL: Very soon after the installation, it became apparent that cement plants also require other arrangements besides the high-dust SCR solution. In addition to our optimisation work on the high-dust SCR system, we developed other variants of low-dust SCR systems. Semi-dust and high-dust systems provide the benefit of an optimum exhaust gas temperature for denitrification from the rotary kiln, while the exhaust gas temperature needs to be increased in low-dust SCR systems. Scheuch has developed additional solutions, such as the SCR tail-end tower, which is a classic clean gas denitrification unit with integrated heat displacement systems using a large plate heat exchanger, and the regenox process, which manages the correct gas temperature levels with integrated recuperator elements. We are also in the process of establishing hot gas filtration systems (using ceramic filter elements) with integrated catalysts. The technological highlight deconox® was developed as a response to new challenges in the cement industry. Cement plants are opening up the possibility of creating a climate-friendly circular economy in the future, partly thanks to lower production costs gained from substituting primary standard fuels with secondary fuels, and partly through the use of alternative raw materials, which is making it possible to conserve raw material deposits. Sophisticated approaches to optimising production processes (based on the use of fuel and a mix of raw materials) require flexible solutions relating to systems designed to reduce emissions. Using alternative raw materials naturally leads to different emission values, which do not necessarily have to be managed in the rotary kiln. The use of an exhaust air cleaning technology that takes over this task offers an enormous economic advantage due to the flexibility it delivers. Scheuch has taken this fact into account in its deconox process. This combines regenerative thermal oxidation (RTO) with a low-dust SCR – two proven technologies in one system. Deconox uses energy from exhaust air containing pollutants to break down other pollutants such as nitrogen oxides and organic compounds. One of the major advantages of the deconox concept is the stabilisation of kiln operation in the event of varying crude gas concentrations and fuel usage, as the kiln is kept separate from the emission reduction tasks. World Cement BMHR 2022
In 2020, Scheuch developed the regenox process, another method for applying low-dust SCR technology with flexible upgrade possibilities. This is based on the proven deconox technology, but without a combustion chamber: that step is factored into the planning process so that expansion into a fully fledged deconox system can take place later. Our strength is our ability to consistently provide our customers with the very best technology, tailored precisely to their processes.
Can you tell us about any other successful projects?
GL: We have implemented numerous projects in recent years: here are just a few examples of our lighthouse projects. Deconox, a patented process for the combined denitrification and separation of organic compounds, celebrated its premiere in 2016 at Hofmann GmbH’s Kirchdorfer cement plant in Austria. In 2021, a low-dust SCR system was installed at Industria Cementi Giovanni Rossi in Italy. What makes this system special is that the heat exchangers integrated into the SCR reactor to recover the majority of the energy required for heating. The advantage over the high-dust SCR system is that the dust-free exhaust gas allows relatively small catalyst volumes to be used, resulting in long service lives. Over time, Scheuch has developed into a full-service provider in the field of flue gas cleaning. We cover the entire flue gas line with our technologies, bringing many advantages to our customers.
Looking to the future, what are the next steps for Scheuch?
GL: We want to ramp up the work we are doing on our path to becoming a total solution provider for a full range of exhaust gas cleaning and heat recovery technologies, catering to every industry. Becoming a one-stop shop for our customers is a firm goal in our mind; we believe that covering the entire flue gas line from a single source is an enormous advantage for our customers. We also intend to focus on hot-gas dedusting with subsequent denitrification or the development of alternative fuel technologies to avoid or reduce the use of fossil fuels such as natural gas. A lot of our work revolves around further developments in thermal post-combustion and heat recovery or extraction. Our research and development department also deals with CO2 capture and reduction. As well as this, Scheuch’s expertise is being put to valuable use in a joint research project on capturing and
using CO2 from cement plants. As an experienced system manufacturer in environmental technology, Scheuch is involved in developing a new type of CO2 separation technology for converting carbon dioxide into useful raw materials. Scheuch is also making an important contribution to new oxyfuel concepts thanks to its decades of experience in the fields of filtration and exhaust gas cleaning. The oxyfuel concepts in the cement sector are the necessary precursors to carbon capture and place high demands on the plant configuration. Scheuch is playing a pioneering role in this area.
About the author
Georg Lechner knows Scheuch very well and can look back on more than thirty years of experience in the field of exhaust gas cleaning, environmental technology and energy-efficient solutions for the minerals industry and in particular the cement industry. Georg Lechner has held the position of Head of Sales Industrial Minerals at Scheuch since September 2015. Together with his team of experts, he was involved in the development of many technological innovations (such as deconox, emc, xmercury).
AD INDE X 4B Components www.go4b.com
IFC
Doppelmayr www.doppelmayr-mts.com
02
Arodo BVBA www.arodo.com
51
Euromecc www.euromecc.com
63
ATD Abbausysteme GmbH www.atd-cardox.de / www.atd-pgs.com
OBC
Hatch www.hatch.com
17
ATMOS Handling www.atmos-handling.com
71
KettenWulf www.kettenwulf.com
35
AUCBM www.aucbm.net
46
Agudio www.agudio.com
25
Aumund Fordertechnik GmbH www.aumund.com
21
Martin Engineering www.martin-eng.com
09
Axians IAS www.axians-ias.com
55
Mole•Master Services Corporation www.molemaster.com
49
Bedeschi www.bedeschi.com
45
PSCL www.pscl.com
07
BEUMER Group www.beumer.com
OFC
Regal Rexnord www.regalrexnord.com
29
Brelko Conveyor Products www.brelko.com
43
Scheuch GmbH www.scheuch.com
69
CICSA www.cicsa.com
13
Starlinger www.starlinger.com
63
Cintasa S.A. www.cintasa.com
57
Van Aalst Bulk Handling www.vanaalstbulkhandling.com
33
Claudius Peters www.claudiuspeters.com
IBC
Vortex Valves www.vortexglobal.com
57
Cross Wrap Oy www.crosswrap.com
55
Wam Group www.wamgroup.com
39
DCL www.dclinc.com
61
72
World Cement BMHR 2022
Packing Technik
Integrated Technology
Unlock the full potential of your plant with high capacity packing and palletizing from Claudius Peters
ROTO FILL
IN-LINE FILL
ROTO FILL AIR
BAG APPLICATOR
PALLETIZER
BIG BAG FILL
We know how.
claudiuspeters.com
n Packing weights of 25kg and 50kg n Compact, modular, easy to install n Energy efficient n Superior packing plant technology n Innovative turnkey solutions n Lower maintenance costs n Custom designed solutions n Global support network n Over 13,000 bulk materials evaluated in Claudius Peters Technikum T: +49 4161 706-0 E: info@claudiuspeters.com Cooling | Grinding | Packing | Pneumatic Conveying | Silo Systems | Stockyard Systems | Marine Powder Handling | Turnkey Systems A Langley Holdings Company.