
The science fueling the next generation of hydration
Commercial Banking
The pace of modern retail is relentless. From stock management and working capital to customer experience and expansion, every decision affects the next.
At Nedbank Retail Services, we combine deep sector expertise with practical, specialist guidance and faster decision-making. We offer solutions that are built for scale, built for complexity, and built for you.
So, while you’re running the front line of retail, we’re behind the scenes helping you grow, adapt, and lead.
Think bigger. Think Nedbank Commercial Banking.
For more information about our services, email us at KarenKe@nedbank.co.za
Premium sustainable labelling
READY – TO – DRINK
Hydration just got a lot more
34
TOPS AND CLOSURES
A wine bottle rethought from the ground up
36
FLAVOUR INSPIRATIONS
Bold just got a whole lot more structured
Natural fruit preparations and juice concentrates
42
INSPECTION, CODING & MARKING
If it leaves the line, it needs to be right.
EDITORIAL
Editor: Kelebogile Nondzaba +27 (0)78 175 9632 kelebogile.nondzaba@media24.com
Layout & Design: Tumi Kunene
Cover Image and current page: Chatgpt and Getty Images
ADVERTISING
Key Account Manager: Càndida Giambò-Kruger +27 (0) 71 438 1918
càndida.giambò-kruger@media24.com
INTERNATIONAL SALES
Germany/Austria/Switzerland: Eisenacher Medien
Erhardt Eisenacher +49 228 249 9860 info@eisenacher-medien.de
Italy: Ngcombroker
June has been a busy month — in the best possible way. A major industry rebrand, one of the biggest food trade events on the African calendar. An edition that reflects exactly where the industry is right now: innovating, consolidating and pushing to meet a market that keeps raising its expectations.
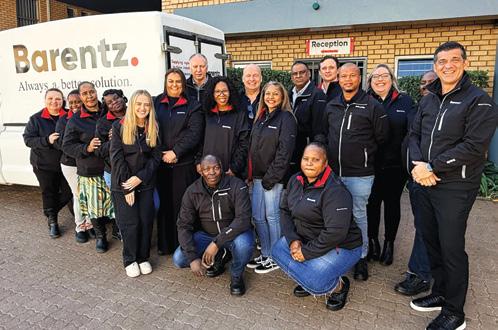
Our Company Focus leads with news that has been building since 2019. SK Chemtrade has been fully acquired and rebranded as Barentz South Africa — an announcement made at the Africa Food Show in Cape Town on 10 June. See page 8
The Food Review team was on the ground at the Africa Food Show 2026 at the Cape Town ICC. More than 8 000 visitors and 350-plus exhibitors across three days confirmed that the appetite for face-to-face industry engagement is very much alive. Read more on page 11.
Our conveyor systems section is a timely reminder that great ingredients mean nothing without the production infrastructure to back them up. Reliable, hygienic and well-maintained lines are what get food from the factory floor to the consumer — and this section gets into the detail of how, turn to page 14 to learn more.
The flavour editorial tracks South Africa’s clear shift away from neutral. Vegetable-led profiles, sweet-heat combinations, smoky BBQ, umami-rich chef-inspired cues and premium seafood inspirations are all gaining traction — in snacks, marinades and seasonings alike, see page 34.
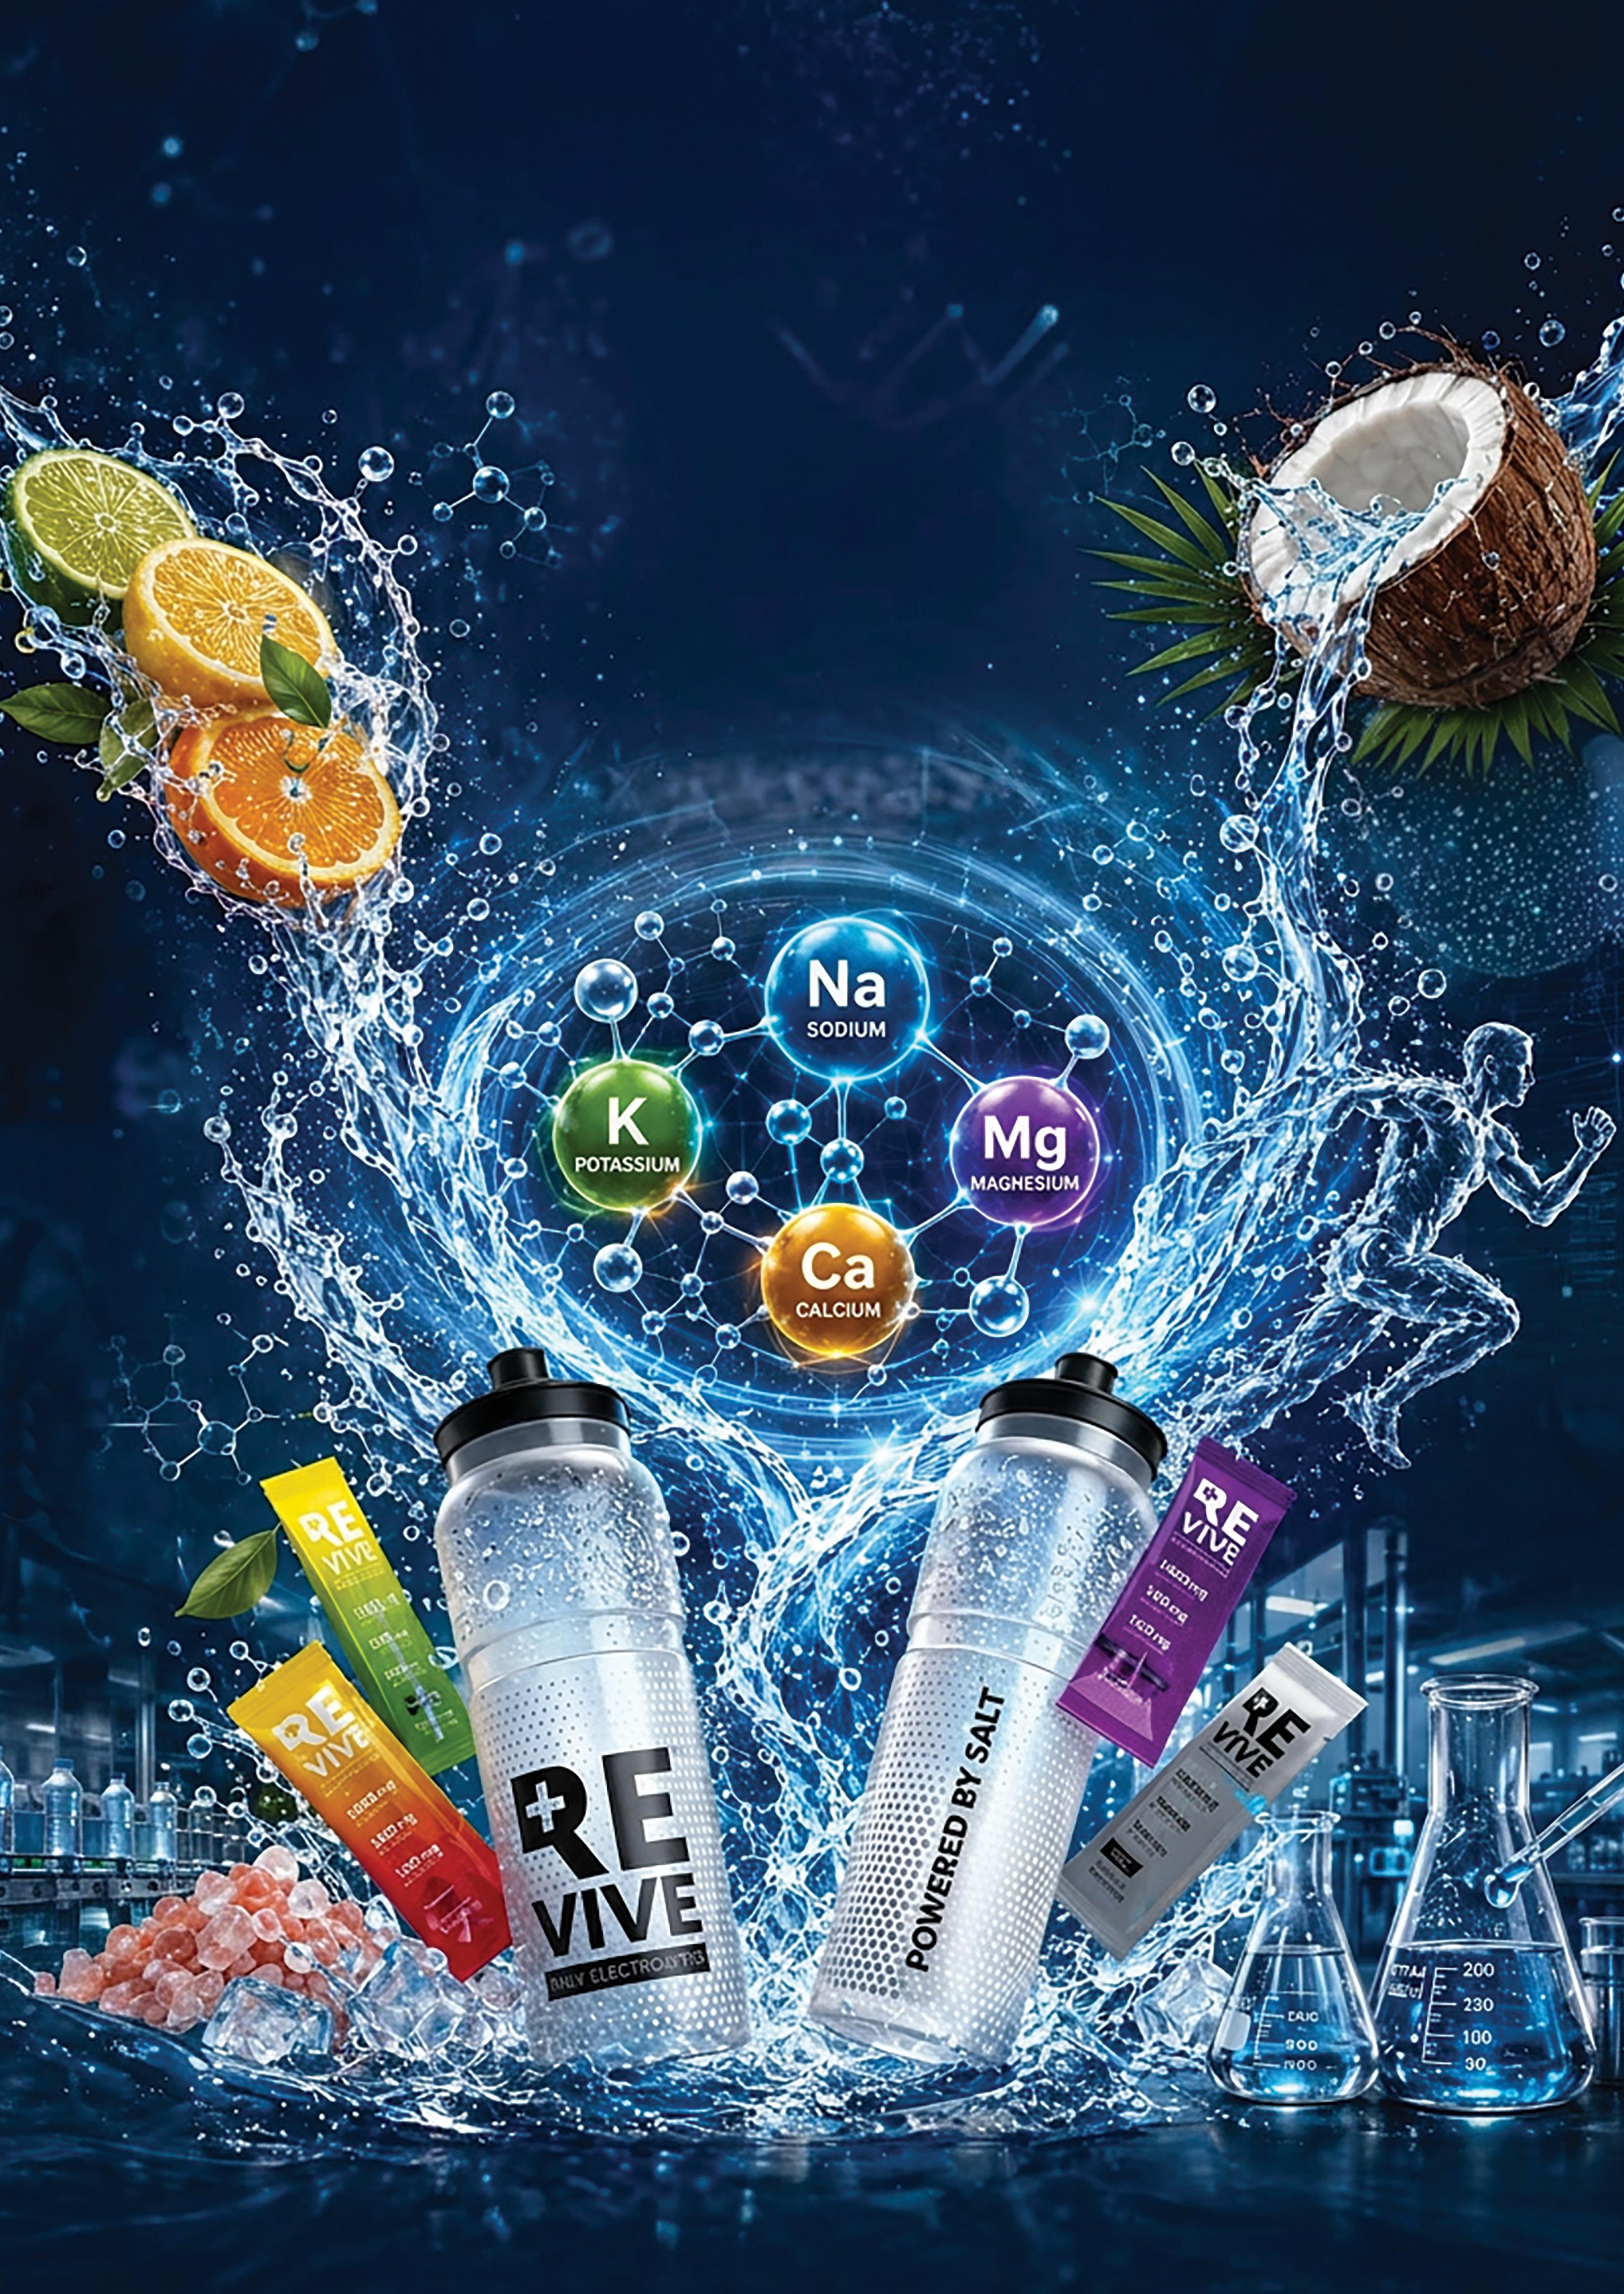
Our cover story on page 30 looks at ready-to-drink functional hydration — a category growing with real purpose. Functional mineral electrolytes such as magnesium, calcium, potassium and sodium are driving formulation innovation for exercise recovery, travel and everyday hydration. The science is solid, and the consumer demand backs it up.
Dig in – let us know what resonates! Kelebogile (Lebo) Nondzaba
Giacomo Rotunno +39 370 101 4694
g.rotunno@ngcombroker.com
Taiwan: Ringier Trade Media
Sydney Lai +886 4 2329 7318 sydneylai@ringier.com.hk
CIRCULATION
Circulation Manager: Rae Morrison Email: Rae.Morrison@media24.com
PUBLISHING TEAM
General Manager: Dev Naidoo
Head of Content & Digital Strategy: Varushka Padayachi
Production manager: Angela Silver
Production Controller: Mandy Ackerman
Group Art Director: David Kyslinger
MEDIA24 MEDIA
CEO: Minette Ferreira
CFO: Lana Goliath
MEDIA24 CORPORATE
CEO MEDIA24: Raj Lalbahadur
CFO MEDIA24: Nelmarie Beyers JOHANNESBURG OFFICE
Building 13, The Woodlands Office Park, 20 Woodlands Drive, Woodmead, Sandton PO Box 784698, Sandton 2146
Tel: +27 (0)11 713 9000
POSTAL ADDRESS PO Box 784698, Sandton, Johannesburg, 2146
COMMUNICATE & CONNECT



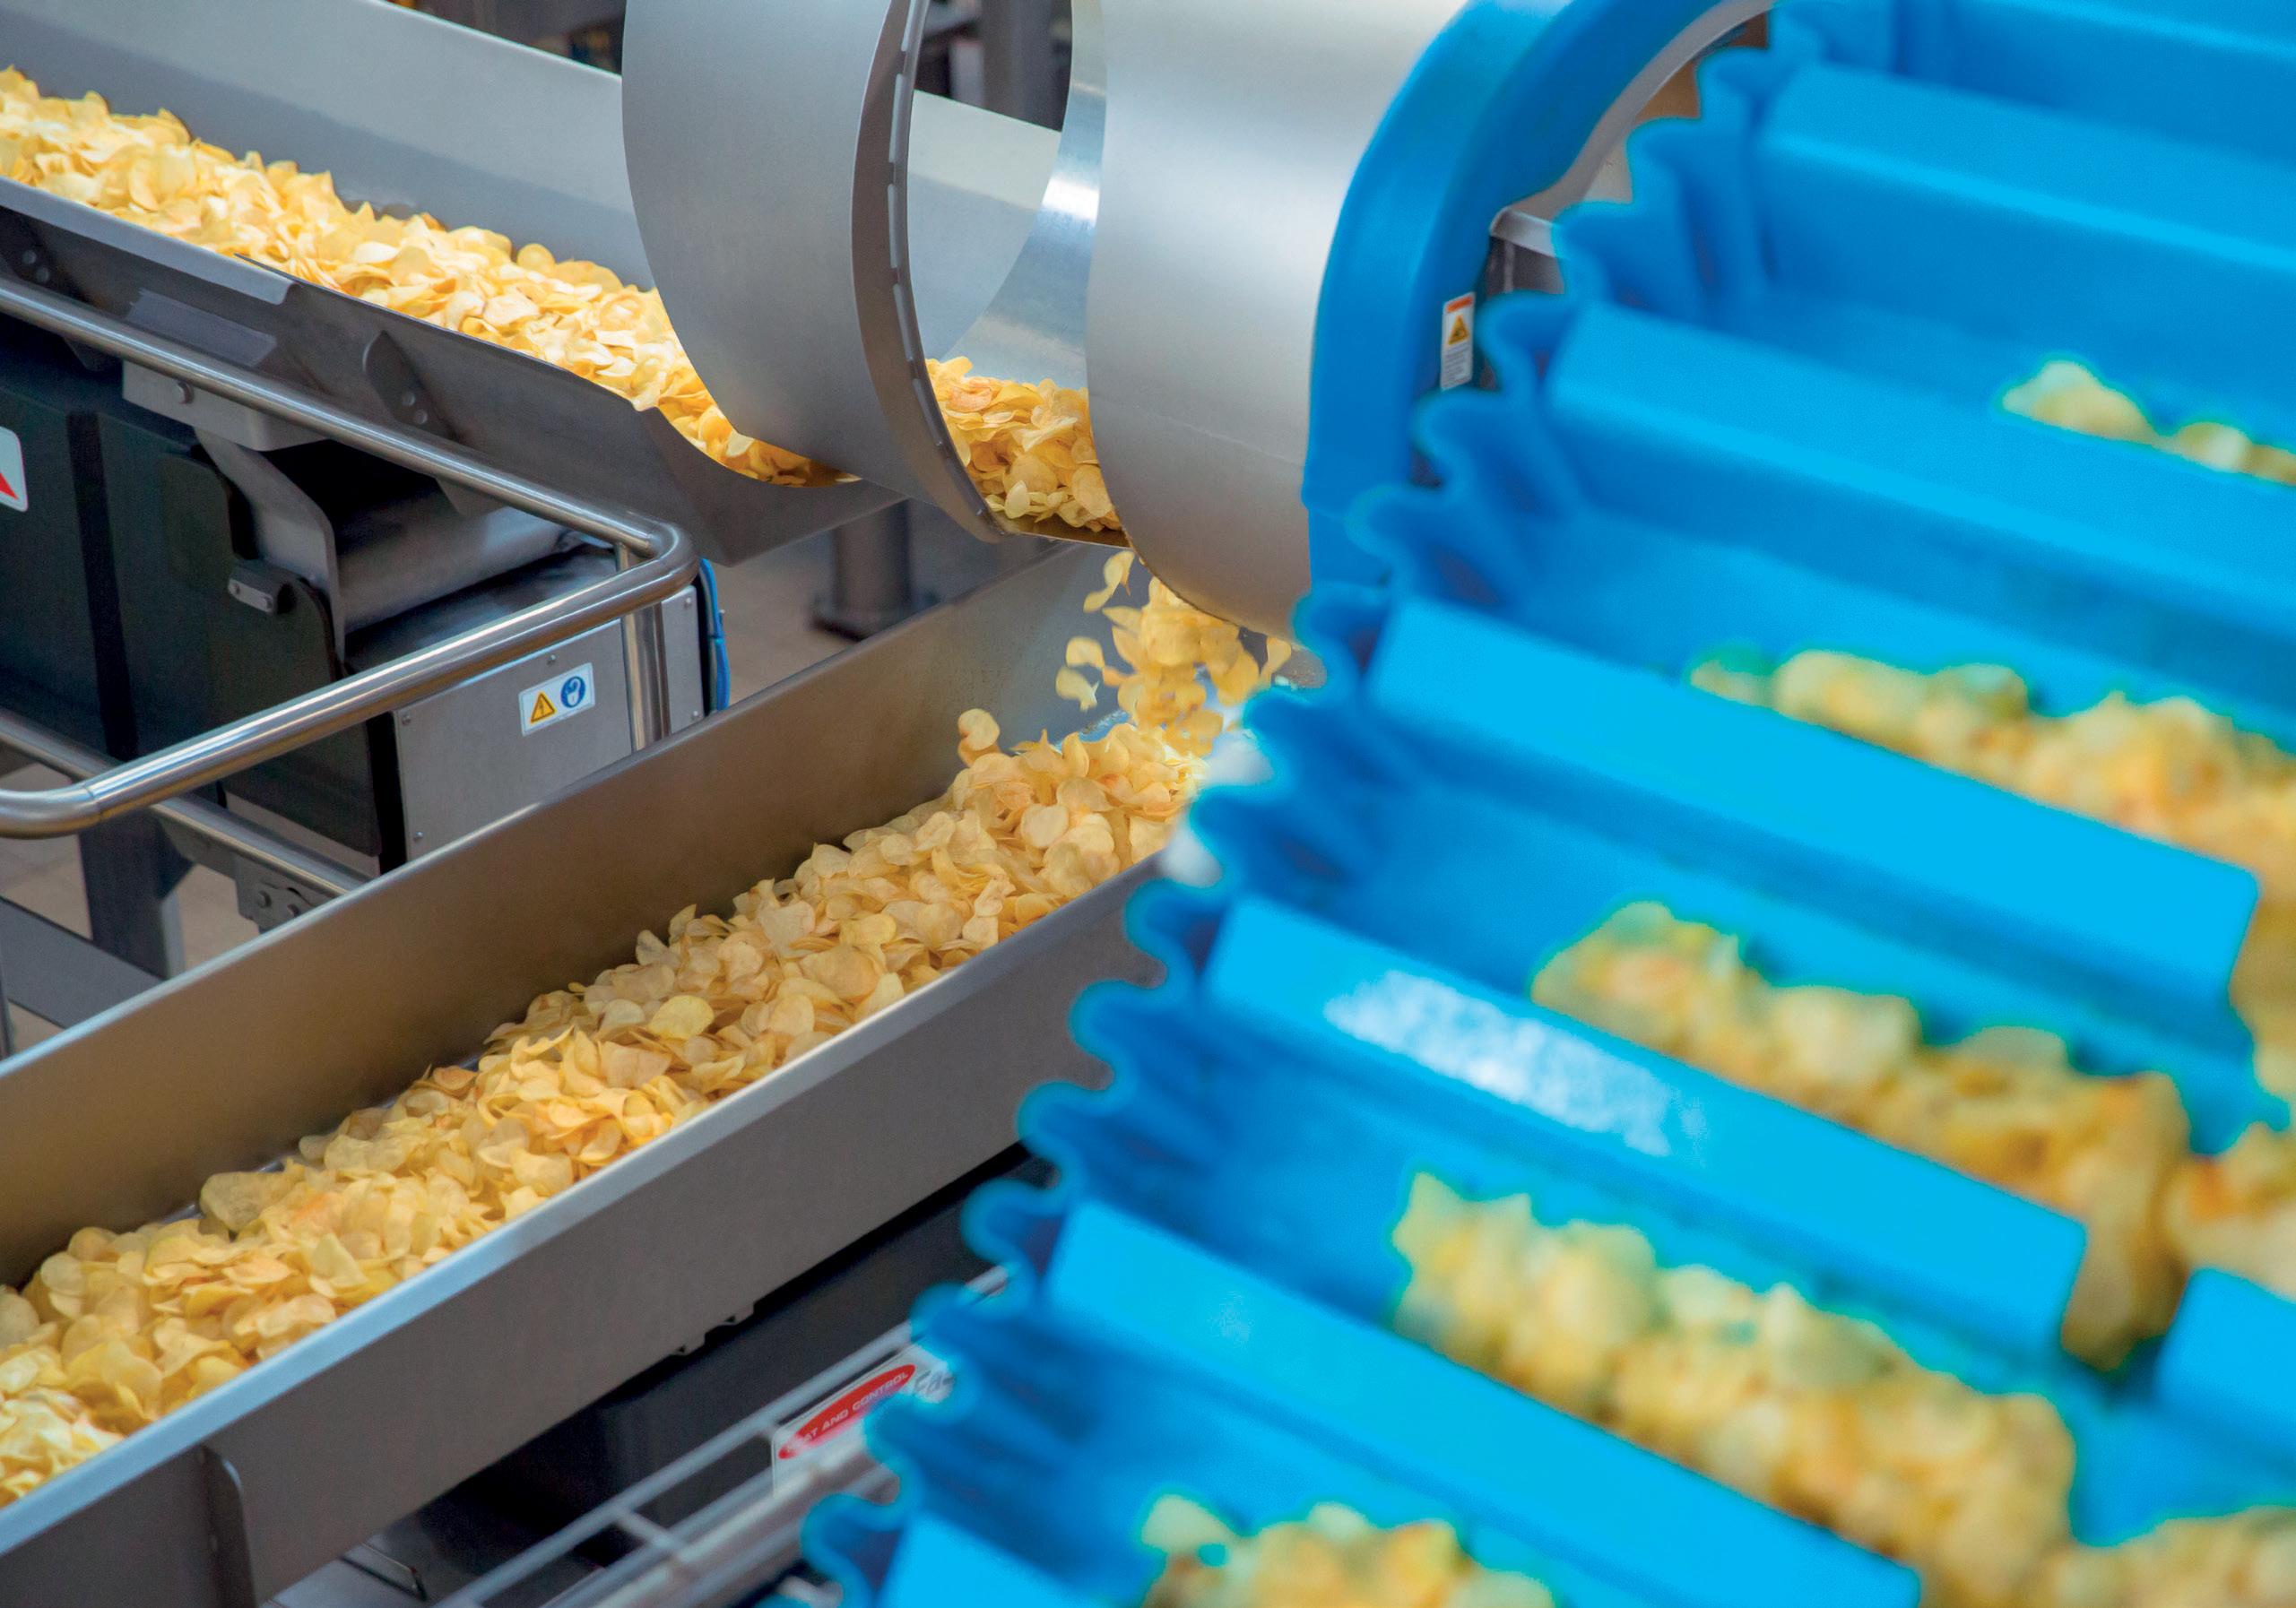
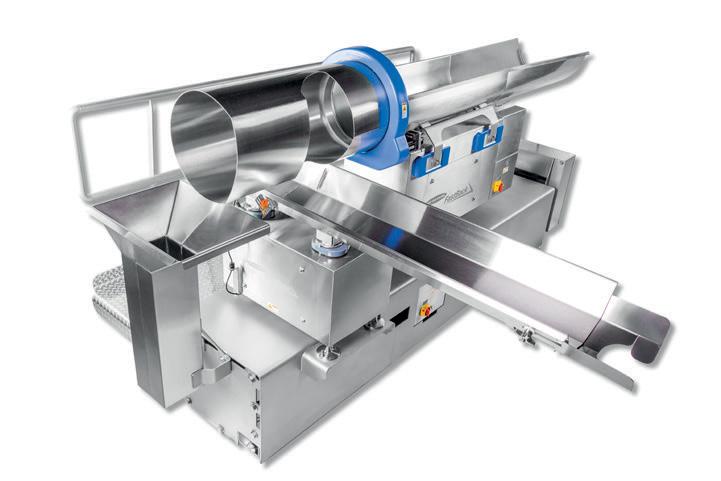
Smart and flexible conveying that keeps your line running smoothly. We provide a wide variety of innovative and dependable conveying and product handling systems to move product through the line as efficiently as possible.
Ideal applications:
• Snack foods
• Prepared foods
• French fries
• Fresh produce
• Pet food
• Nuts & Trail Mix
• Crackers
• Confectionery
LOOKING BACK. PRESSING FORWARD. ALWAYS INNOVATING.
AFMASS Food Expo
15 – 17 July
Kenya & East Africa www.afmass.com
FoodPro 26 – 29 July
MCEC Melbourne www.foodproexpo.com
IFT FIRST Annual Event and Expo 12–15 July
McCormick Place, Chicago, Illinois, USA www.ift.org/ift-first-event
Organic Produce Summit (OPS) 14–16 July
Monterey, California, USA www.organicproducesummit.com
Africa Food Show Kenya 2026
19–21 August
Nairobi, Kenya www.africafoodshow.com
Vietfood & Beverage – ProPack 2026
6–8 August
Saigon Exhibition & Convention Centre www.foodexvietnam.com
Dairytech Africa
9 – 11 September
KICC. Nairobi. Kenya www.dairytechafrica.com
Africa Print Expo
8 – 10 September
Gallagher Convention Centre, South Africa www.africaprintexpo.com
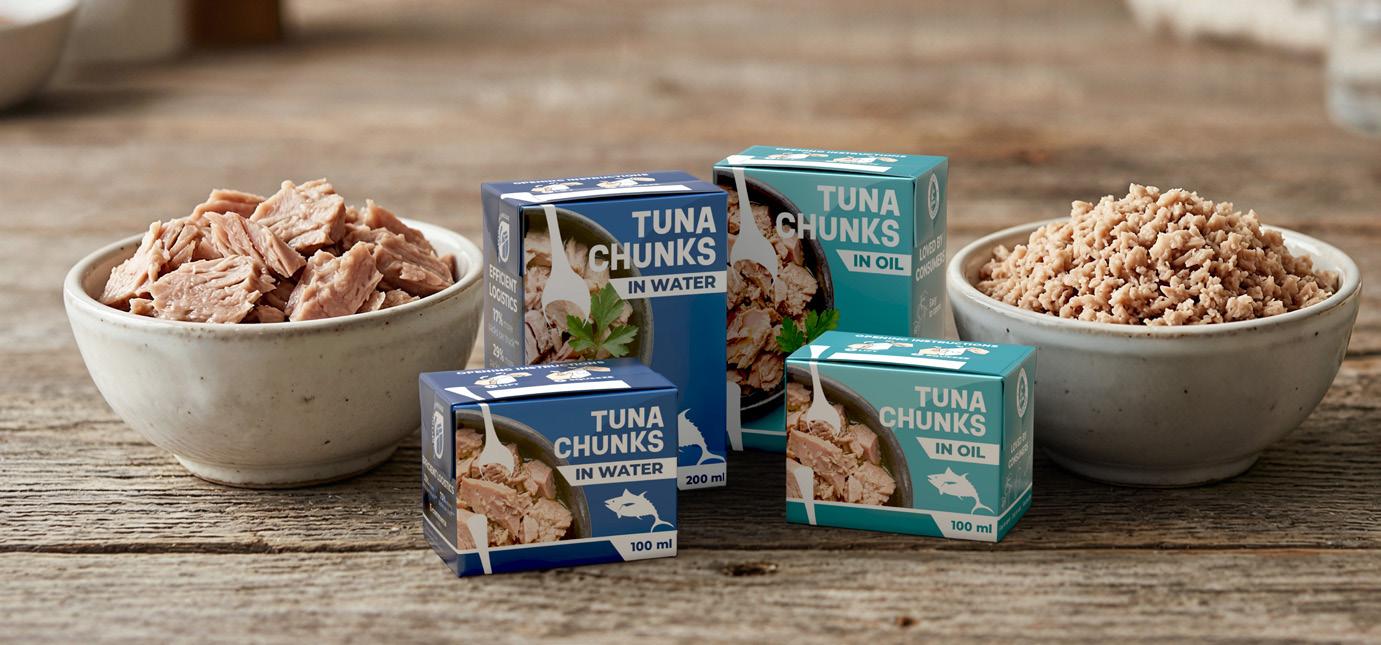
Tetra Pak, in collaboration with the leading Spanish seafood producer Jealsa, has today unveiled the industry’s first carton packaging for shelf-stable tuna. Packaged in Tetra Recart®, this market-leading innovation launched in Sweden last month with retailer Axfood in 200 ml Mini format and will be available to food producers and brands worldwide.
The solution was brought to market in collaboration with the leading Spanish seafood producer Jealsa, combining expertise in food packaging from Tetra Pak with decades of experience in producing high-quality seafood products at Jealsa.
A unique paper-based alternative to tradi-
tional cans, Tetra Recart offers food producers a new way to differentiate in one of the seafood industry’s most established categories. The global shelf-stable tuna market is expected to grow an estimated 12% to 12.4 billion units by 2030, reflecting rising demand for affordable, versatile and long-lasting protein options.1
Tetra Recart offers brands a cost-competitive, scalable paper-based packaging solution and already supports a wide range of shelf-stable products, from spreads and flakes to shredded tuna and chunks, with plans to expand into additional tuna preparations as the category evolves.
Southern African manufacturers are facing unprecedented operational pressures, from rising labour costs to growing demand for processed foods. To meet these challenges, companies are turning to automated solutions on the factory floor, and the partnership between Yaskawa Southern Africa and Dale Automation effectively demonstrates how robotics and material-handling expertise can transform end-of-line operations. Across the region, manufacturers are grappling with labour costs and the challenge of maintaining efficiency in high-volume production. “Over the long run, the cost of capital equipment continues to decrease while labour costs rise,” explains Jan ‘t Hart, National Sales Manager at Yaskawa Southern Africa, highlighting why automation is increasingly attractive.
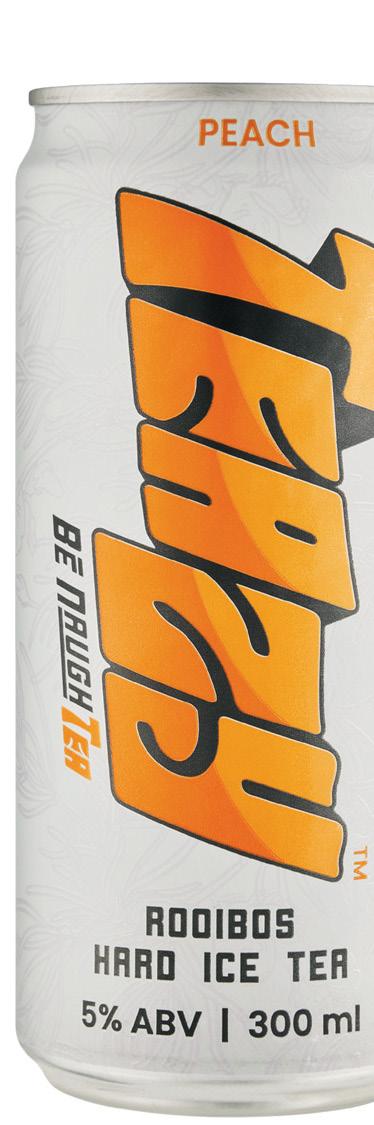
From the southern tip of Africa to the top of the world, Teazy Peach Rooibos Hard Ice Tea has been named World's Best Spirit & Mixer at the prestigious 2026 World Premix Awards, beating some of the biggest names in the drinks industry to secure the category's highest accolade.
Judged under the internationally respected World Drinks Awards programme, the World Premix Awards are regarded as the global benchmark for readyto-drink and pre-mixed beverages. And, Teazy’s award haul was no small feat, including:
• World's best spirit & mixer –Teazy Peach Hard Ice Tea
• Style winner – Teazy Peach Hard Ice Tea
• Gold medal – Teazy Peach Hard Ice Tea
• Silver medal – Teazy Lemon Hard Ice Tea
The judges’ feedback highlighted its "well-balanced mouthfeel.
HEINEKEN Beverages’ distinguished wine portfolio delivered an exceptional performance at the 2026 Investec Trophy Wine Show, earning an impressive collection of trophies, gold and silver accolades across its leading brands, including Nederburg and Durbanville Hills.
Demand for palletising robots has risen sharply over the past few years, driven by changing eating habits, population growth, and the acceleration of processed food consumption, from mielie meal to pasta and bread.
The results underscore the group’s commitment to producing world-class South African wines across a wide range of styles and price points, with standout performances led by Nederburg’s trophy-winning wines. Nederburg Leads with Double Trophy Success
Nederburg emerged as one of the competition’s top-performing producers, securing two major trophies for its acclaimed Winemasters range.
The Nederburg The Winemasters Noble Late Harvest 2018 achieved a remarkable 98 points and won:
• Trophy for Best Museum Class Dessert Wine
• Trophy for Best Museum Class Wine Overall
The winery’s celebrated The Winemasters Shiraz 2024 further impressed judges, earning 97 points alongside:
• Investec Trophy for Best Shiraz
• Investec Trophy for Discovery of the Show –Best Value Gold Medallist
Additional highlights for Nederburg included:
• Heritage Heroes The Brewmaster Bordeaux Blend 2021 – Gold, 96 points
• Heritage Heroes The Anchor Man Old Vine Chenin Blanc 2024 – Silver, 91 points
• Baronne 2024 – Silver, 91 points.
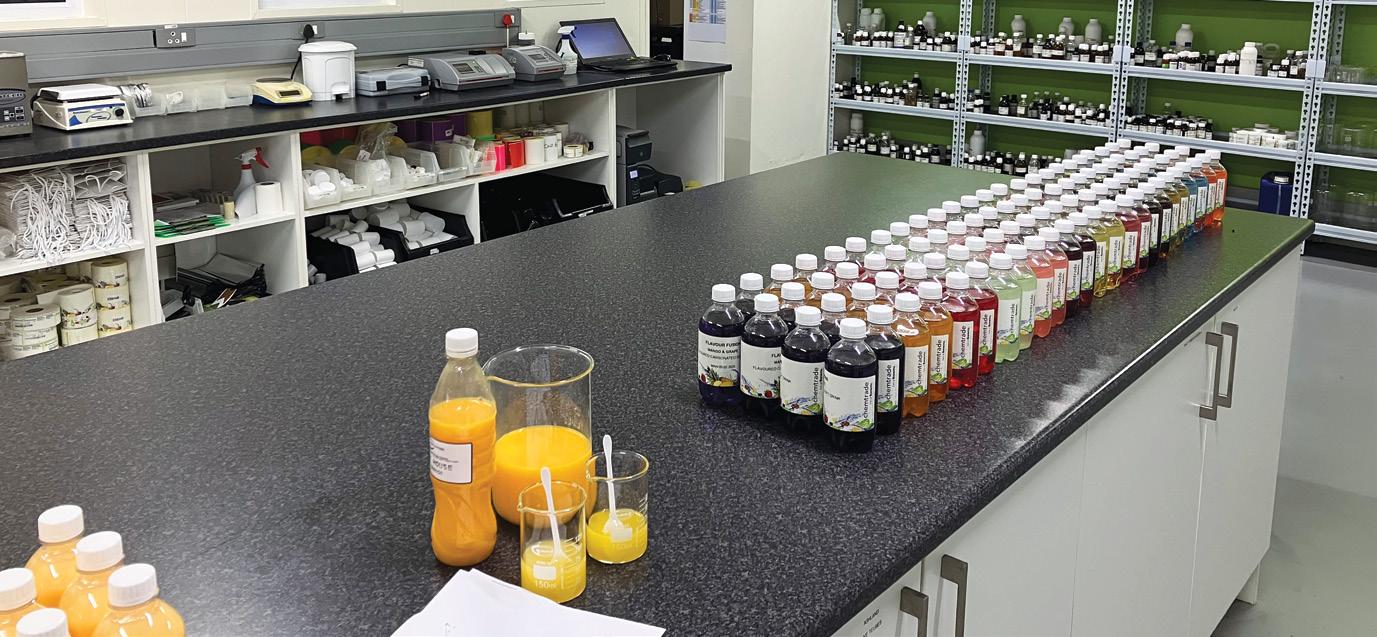
SK Chemtrade has rebranded as Barentz South Africa following a full acquisition by global specialty ingredients leader Barentz — bringing world-class resources, ESG credentials and an expanded product basket to South African customers, by Kelebogile Nondzaba
Barentz, a leading global specialty ingredients solution provider, made its big announcement at the Africa Food Show in Cape Town on 10 June 2026 — confirming the full acquisition of SK Chemtrade Services (Pty) Ltd and the official rebrand to Barentz South Africa.
The relationship between SK Chemtrade and Barentz is not a new one. The two companies formed a joint venture in 2019, signing their agreement in the Netherlands in August of that year, and have since built a track record of strong growth and expanded capabilities. Now, with Barentz taking full ownership, that partnership has entered its most significant chapter yet.
“This transition represents an exciting new chapter for our business,” says Mark Ferrao, Managing Director of Barentz South Africa.
“While our name is changing, our commitment to our customers, partners and service excellence remains exactly the same.”
For Kees Schepers of Barentz, the decision to partner with SK Chemtrade was never purely commercial — it was about cultural alignment. Schepers, who was heavily involved in Barentz’s expansion from a European operation into a global business, recalls a pivotal visit to Cape Town in 2018.
“For Barentz, it’s very important that there’s a DNA match,” he explains. “I travelled extensively with our former CEO and he and I were in Cape Town in 2018 for our first meeting with the SK Chemtrade team. It immediately felt right — the way of doing business, the values, the people. We met Mark, Colleen and Derek, and had a very
“While our name is changing, our commitment to our customers, partners and service excellence remains exactly the same.”
good connection from the start. That was the right basis to continue discussions.”
That connection culminated in the signing of the joint venture agreement in August 2019 in the Netherlands. Barentz, founded in 1953, remained a predominantly European business until 2010, when it began expanding into Asia, then India, South America, South Africa, Central America and the United States — ultimately becoming a true global player in specialty ingredients distribution.
With seven years having passed since the joint venture was formed, the question of timing is a natural one. Why formalise the full
acquisition now? Both Ferrao and Schepers are clear: the South African market has matured to the point where it can fully absorb and benefit from what a global Barentz entity has to offer.
“Five or six years ago, we weren’t ready for it,” says Ferrao candidly. “Our market wasn’t ready for it. But today, our customers are educated, they’re asking the right questions, and they want access to the global product basket that Barentz has from its principals. The footprint is now here to deliver that.”
Schepers adds that globalisation and the growing importance of emerging markets have also shaped Barentz’s internal thinking.
“What we’ve seen happening in the world over the last few years has shown us that footprint into emerging markets is critical. South Africa was always the right fit — it was simply a matter of the right timing for both sides.”
The choice to use the Africa Food Show as the platform for the rebrand announcement was deliberate. For a company stepping onto a global stage, the show offered
"In distribution, you must make two people happy: your principal partner and your customer. The emerging markets are the perfect place in the world right now for growth — but you won’t achieve that without a customer who receives real value from what you’re adding, value add is everything.”
decision-makers, customers and peers, all in one place.
“This is Africa’s best event to be able to showcase what we’re doing and to tell the market about our rebrand,” says Schepers. “The quality of the show is improving and it’s getting bigger each year. That accelerated growth mirrors what we are doing ourselves, and it felt like the right occasion
As South African consumers become more informed and more demanding, sustainability has moved from a nice-to-have to a non-negotiable. Barentz South Africa is well positioned to meet that demand, backed by the group’s global ESG framework and its Ecovadis gold-status sustainability rating — with just one level remaining to achieve the highest possible score.
“We have a global logistics system in place, and we understand the concerns around carbon footprint and environmental impact,” says Schepers. “The global ESG framework that Barentz has built is something we want to make available locally. We can offer our customers the supplier claims they need — proof that their ingredient supplier is ESG-performing on a global level. Barentz is that partner.”
Ferrao was quick to point out that ESG is not only a Barentz level initiative but also from our Principal partners, such as IFF and Oterra. “It’s not only from a Barentz perspective — our supplying partners also have ESG at the forefront of their thinking. Companies like Oterra and IFF are sustainable on a global
initiative, and it’s very important to have ESG front of mind across the entire value chain.”
Schepers adds that Barentz’s Ecovadis rating is automatically extended to Barentz South Africa as a wholly owned entity — a significant credential for local customers seeking globally recognised ESG assurance from their suppliers.
One of the tangible benefits of the full acquisition is access to Barentz’s global logistics infrastructure and its proactive procurement model — a system that sets it apart from many in the local distribution market.
“We work six months ahead at any given time, and we hold three months’ worth of stock,” explains Ferrao. “We can see the peaks and troughs coming before our customers do. We work ahead of what they anticipate, based on historical data and a three-year model, and we’re able to tell them what they need, when they need it and how they need it. That’s a level of service that not everyone in this industry offers.”
This forward-planning approach is particularly valuable in the South African context, where supply chain disruptions — from port delays to air freight challenges — can derail production schedules. Having global reliance and a proactive system in place means that customers are insulated from those disruptions before they even become a problem.
Asked about the ingredient categories of the future, Schepers does not hesitate. “Looking at what’s trending, it’s very much nutraceuticals and biopharma,” he says. “Those aren’t single ingredients as such — they’re ranges of products, categories in their own right. We need to serve our nutraceutical customers and our biopharma customers, and that is very much where our focus is going.”
Ferrao agrees, and frames it in the context of a consumer base that has fundamentally changed. “The days where a product just had to taste good are gone,” he says. “Consumers want functional. They want value add. Whether it’s what goes into a child’s lunchbox or what sits on a retail shelf, it has to deliver something beyond flavour. And sourcing matters too — people want to know where their ingredients come from and whether they’ve been sourced responsibly. That transparency is no longer optional.”
To support this, Barentz operates on a principal-based management model, care-
Barentz was founded in 1953 and expanded out of Europe in 2010 — it now operates in over 20 countries across Asia, India, South America, Central America, Africa and the US.
fully selecting the partners it represents and serving them on a global scale. Where additional sourcing is required, the company deploys dedicated auditing and a global quality assurance team to ensure full trackand-trace capability back to source.
Despite the significance of the rebrand, both Ferrao and Schepers are emphatic that, for customers, the experience will be one of continuity. All existing relationships, agreements and projects continue seamlessly. The management team remains in place. The address has not changed. What has changed is the scale of the resources, the breadth of the product basket and the depth of the global support structure behind the local team.
The rebrand to Barentz South Africa also unlocks new business pillars that SK Chemtrade could not previously offer — including personal care and life sciences — with further pillars planned for the years ahead. The five-year vision is clear: to deliver in South Africa and across southern Africa the same breadth of service that Barentz provides in Europe and other developed markets — but with local expertise, local relationships and a locally embedded team.
“The legacy that SK Chemtrade has left behind is an incredible platform for Barentz to take into the future,” says Ferrao. “We have the same team, the same address, but now with a global mindset. We are FSSC 22000 food-safety accredited — that’s
what our customers have come to expect locally, and now we can offer them that same standard on a global scale, made available right here.”
It’s a compelling proposition: the trust and track record of a well-loved local business, now backed by the resources, reach and reputation of a global leader. For South Africa’s food and beverage industry, Barentz South Africa arrives not as a stranger, but as a familiar face with a far bigger network behind it.

No disruption: All existing relationships, agreements and projects continue seamlessly
Same team: Management and staff remain unchanged
More products: Expanded global product basket from international principals
New pillars: Personal care and life sciences added to existing food and beverage offering
ESG support: Global Ecovadis-rated ESG framework now available locally
Smarter supply: Proactive procurement system — six months planning horizon, three months stock held
Quality assured: Global quality assurance and auditing teams with full track-andtrace capability
Growth regions: Expansion planned across South Africa and into southern Africa.
Barentz South Africa holds Ecovadis gold status for sustainability — with just one rating level left to achieve.
- Barentz –www.skchemtrade.co.za
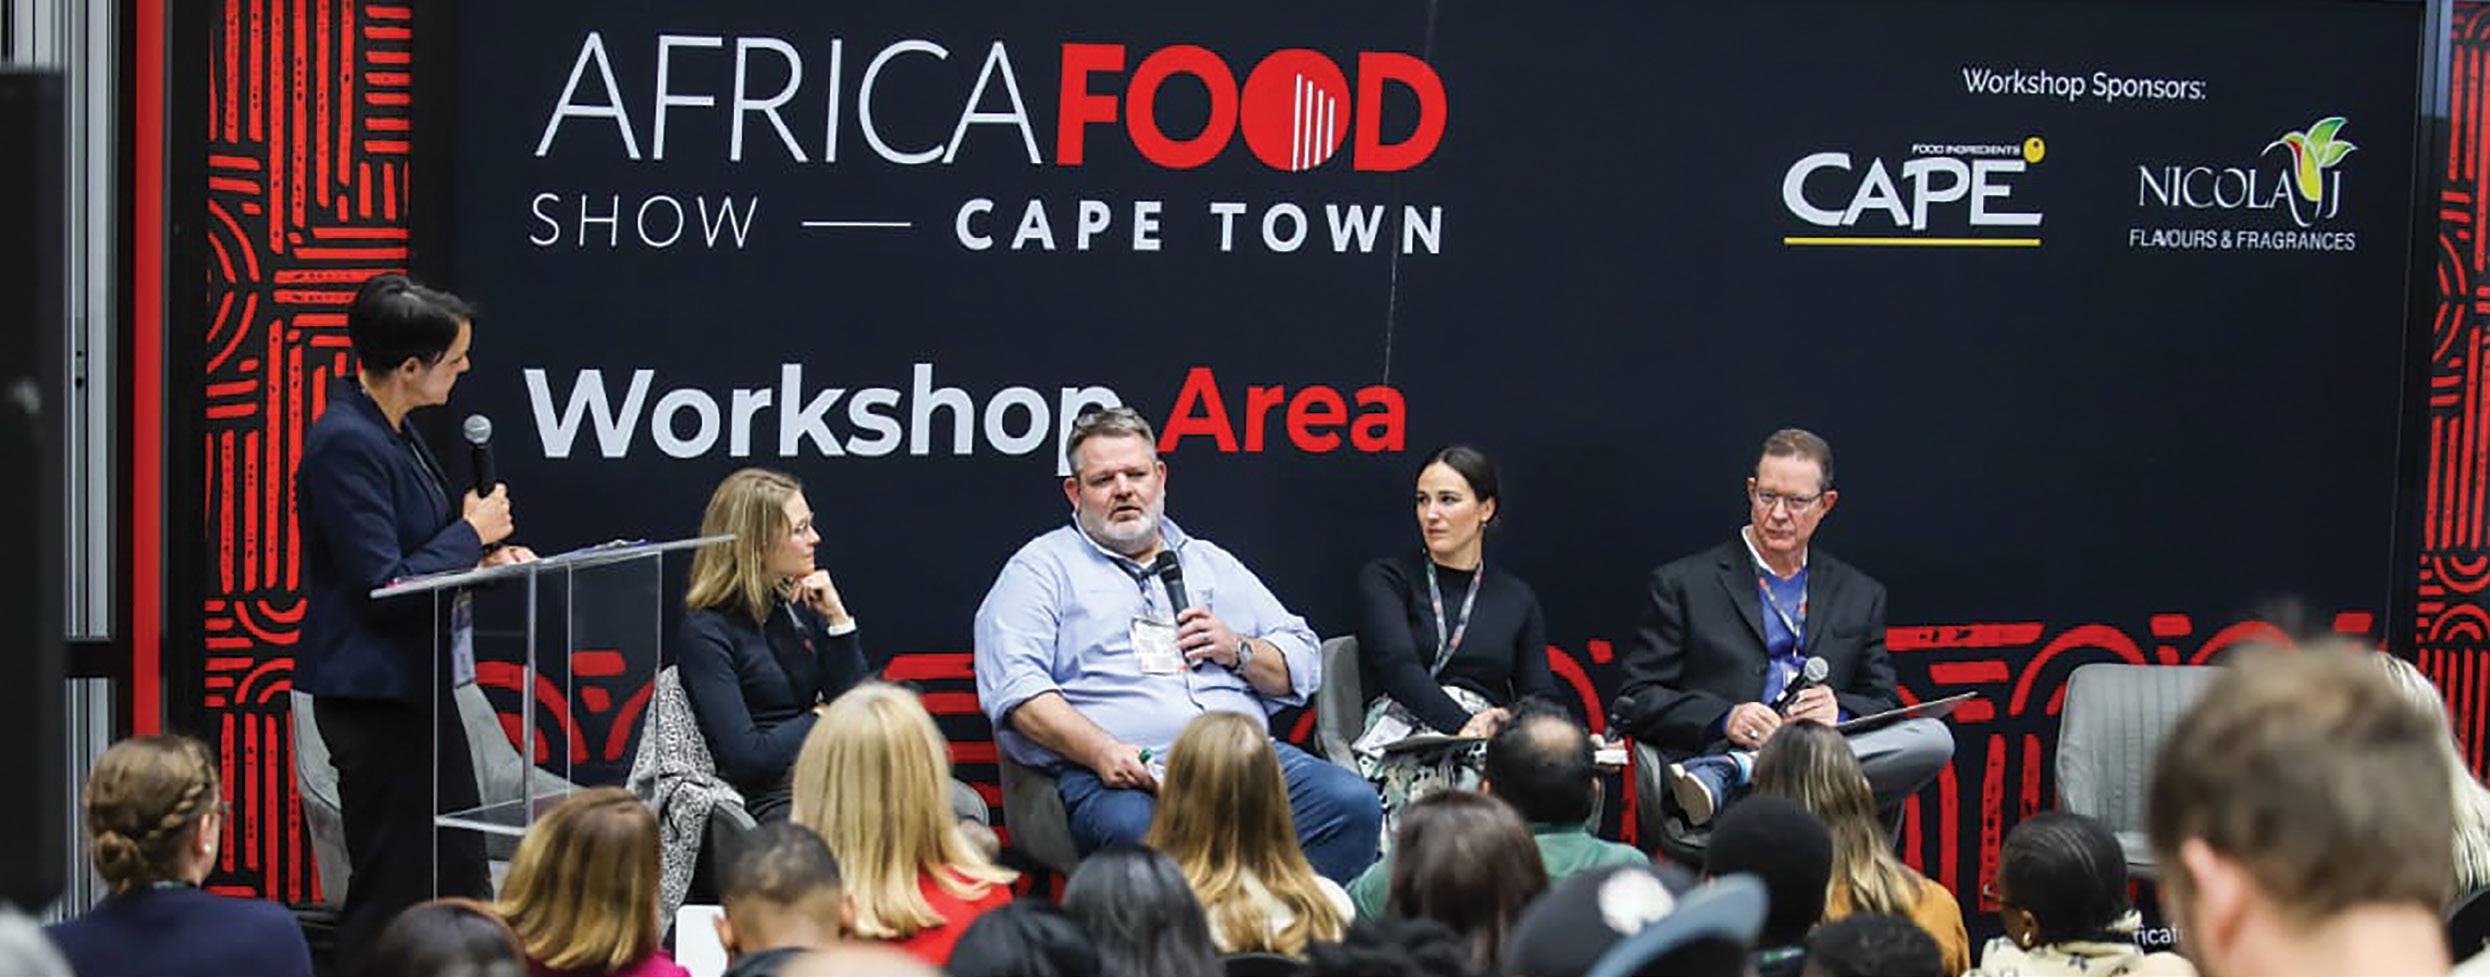
The Food Review team attended the Africa Food Show 2026 which brought about 8 000 visitors, 350 exhibitors and Africa’s food
and beverage industry together in Cape Town.
Africa Food Show 2026, Africa’s premier global food and beverage sourcing expo, concluded its threeday run at the Cape Town International Convention Centre from 10—12 June 2026. Buyers, chefs, food entrepreneurs and industry leaders gathered at the continent’s leading food and beverage sourcing event, where local buyers sourced both local and global product ranges from international and domestic exhibitors. Africa Food Show 2026 placed live expo experiences at the heart of its programme — and delivered on that promise across all three days.
The show opened with an address by Hon. Minister Ivan Meyer, Minister of Agriculture, Economic Development and Tourism, Western Cape Government, who shared insights on how strategic policy, innovation and inclusive market access can drive sustainable growth while strengthening food security across Africa.
“I am pleased to have opened the Africa Food Show 2026 [C1], a platform that brought together innovation, enterprise and practical opportunity for the food and beverage sector. Events like this are vital for strengthening market access, supporting industry growth and building a more resilient food system for the Western Cape and the wider continent,” said Dr Ivan Meyer, Minister of Agriculture, Economic Development & Tourism, Western Cape Government.
With more than 8 000 [C2] visitors through the doors, the show floor was where sourcing happened. Suppliers, chefs, buyers and brand teams from local and international markets
“Taste, source and be inspired — Africa Food Show delivered.”
met to test products, assess packaging and negotiate directly with exhibitors, turning discovery into immediate procurement opportunities.
Across the show floor, visitors tasted product applications from more than 350 exhibitors spanning ingredients, beverages, bakery and convenience food, sourcing both South African products and global ranges from international exhibitors. Africa Food Show proved to be the one-stop sourcing destination for the food and beverage sector.
“Africa Food Show delivered real value in one place, from live culinary competitions and product showcases to practical workshops and direct access to suppliers. We were delighted to welcome buyers, chefs and industry professionals who connected, learned and discovered new opportunities across the food and beverage sector,” said Margaret Peters, Event Director, Africa Food Show.
Alongside the competitions, visitors tasted product applications from more than 350 exhibitors spanning ingredients, beverages, bakery and convenience food, assessed packaging and negotiated directly with suppliers, turning discovery into immediate procurement opportunities.
Africa Food Show 2026 was co-located with Hotel & Hospitality Expo Africa — giving food and beverage suppliers direct access to hospitality, foodservice and retail buyers under one roof.
Workshops and thought leadership sessions ran alongside the live expo experiences, offering 10+ practical sessions and panels over the three days, focused on product development, sourcing strategies and commercial growth. Each session delivered takeaways that visitors could apply on the production floor or shelf.
“Synercore is proud to have supported [C6] the Africa Food Show, bringing industry expertise and scale to accelerate innovation and commercialisation across Africa’s food value chains,” said Dr Tertius Cilliers [C7], CEO of Synercore.
Co-located with the Hotel & Hospitality Expo Africa, the two events created valuable crossover opportunities, with a steady stream of relevant buyers and decision-makers from the broader hospitality, foodservice and retail sectors moving between the shows.
AFRICA FOOD SHOW 2026 — BY THE NUMBERS
• 8 000+ Visitors over three days
• 350+ Exhibitors spanning local and international markets
• 10+ Practical workshop sessions and panels
• 4 Live culinary competitions and experiences
• 3 Days at the Cape Town International Convention Centre
• 1 Platinum Sponsor: Synercore
• Free Entry for all registered visitors
• Co-located With Hotel & Hospitality Expo Africa for maximum crossover value
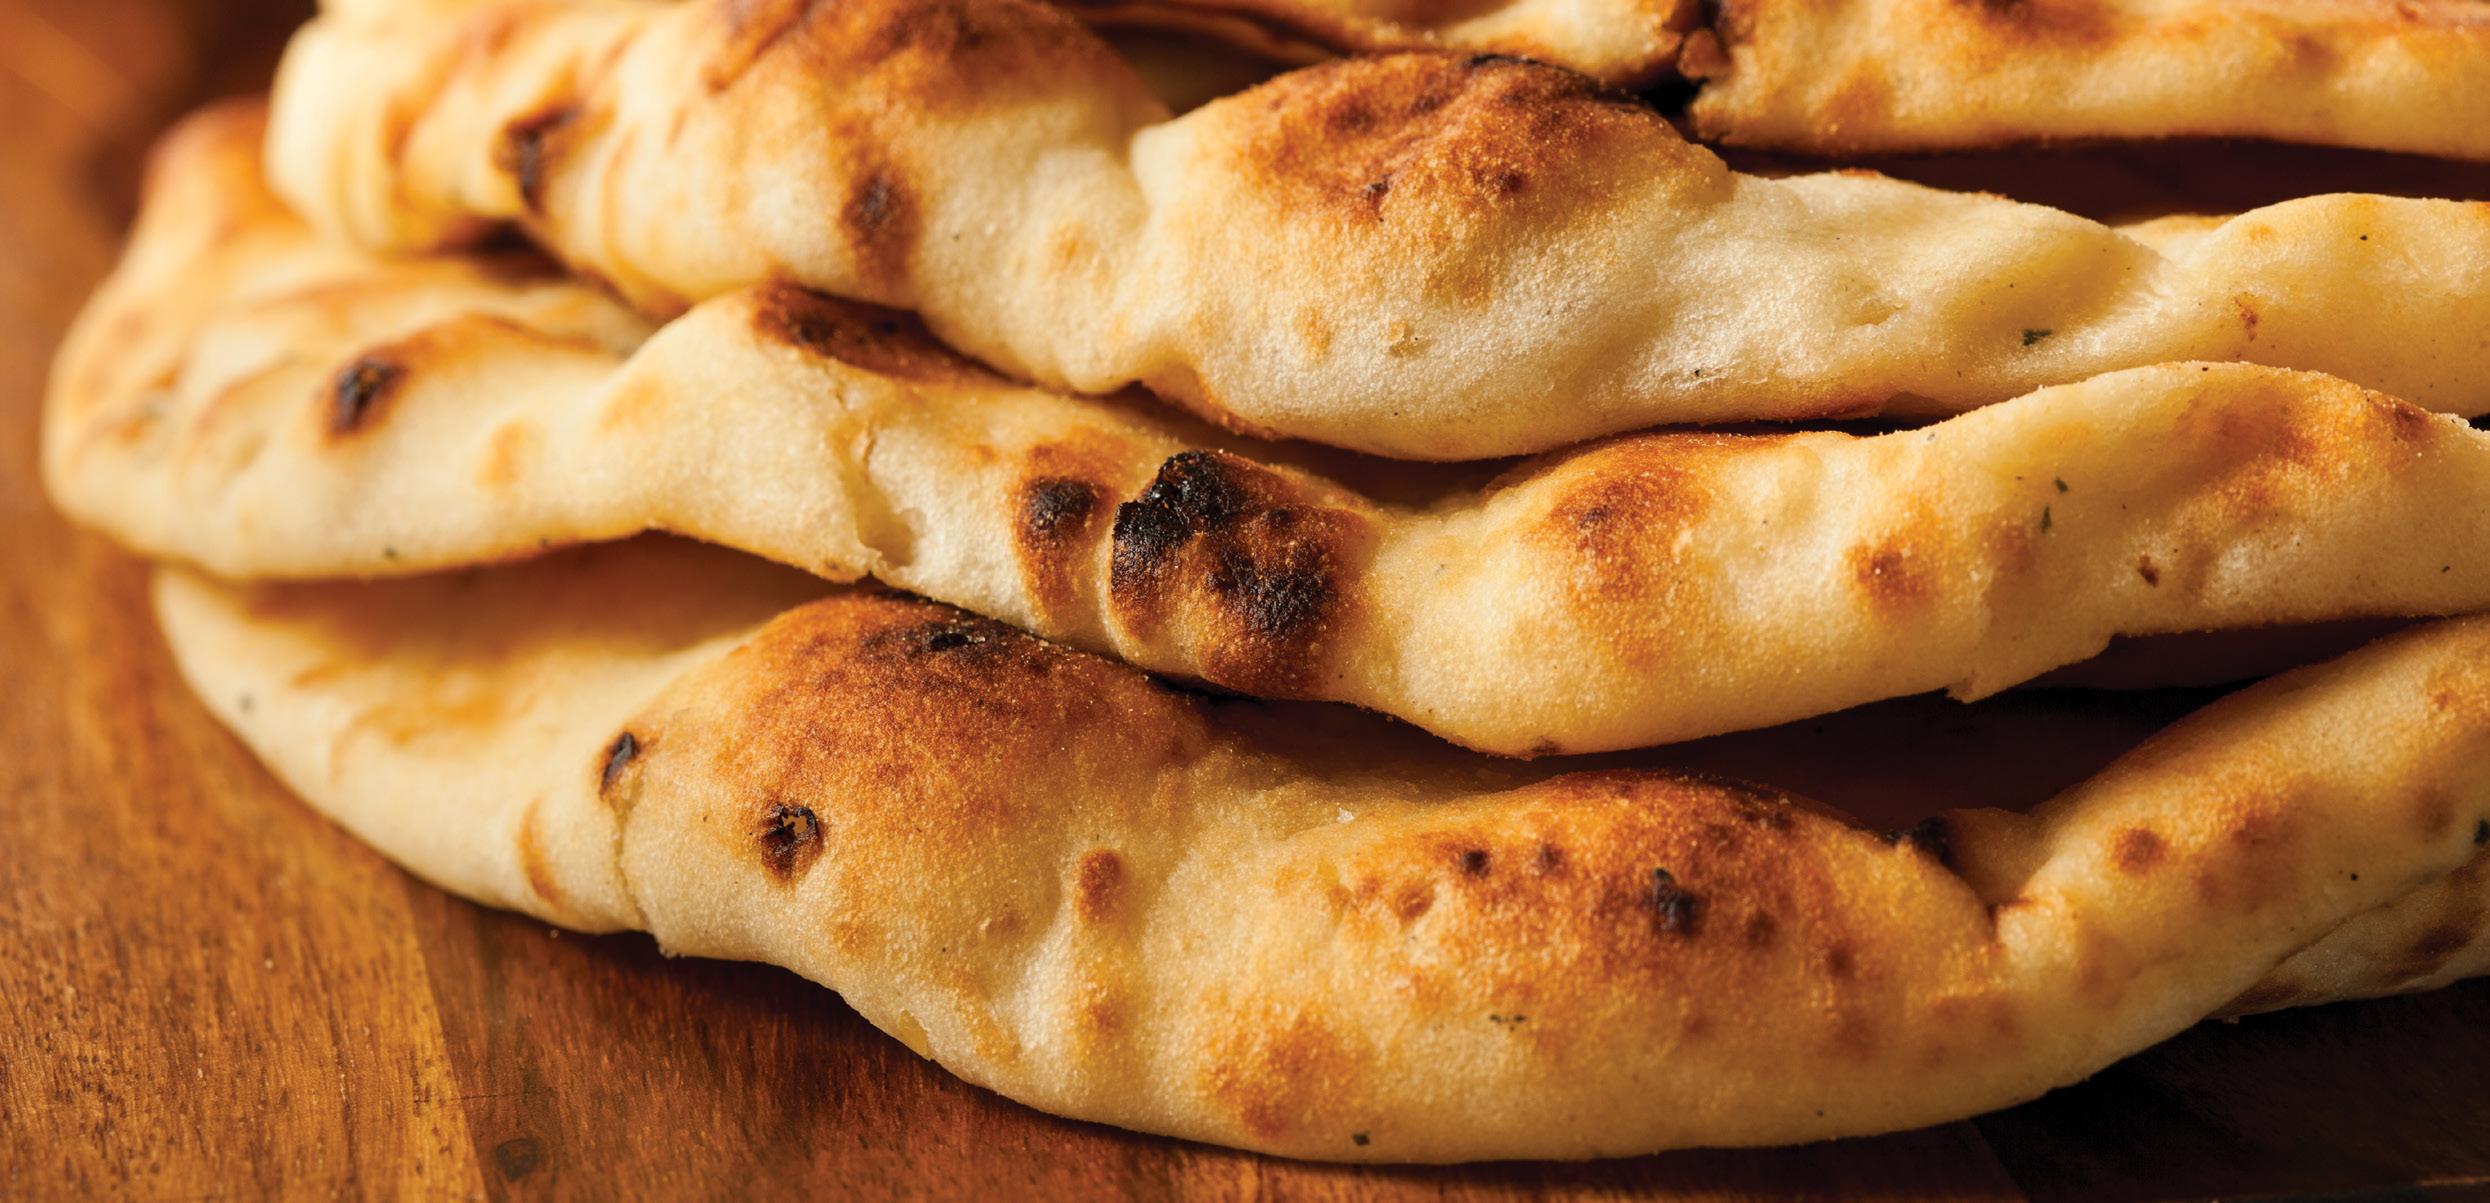
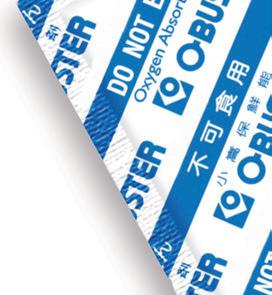
In today’s competitive bakery market, manufacturers are expected to deliver products that maintain freshness, quality and consistency from production to consumption. Whether supplying retail chains or foodservice distributors, shelf life remains one of the most important commercial considerations in bakery production. Products such as gluten-free bread, traditional biscuits, packaged rotis and brownies with high fat content each present their own preservation challenges. Moisture migration, oxidation, flavour loss, textural changes and microbial spoilage can all reduce product quality long before the intended best-before date. For bakery manufacturers looking to improve product stability without compromising formulation, O Buster Oxygen Absorbers provide an effective packaging solution that actively protects products against one of the biggest causes of quality deterioration — oxygen.
Even after a product has been baked, cooled and sealed, oxygen remains present inside the package headspace. In some cases, oxygen
“Oxygen is a major factor limiting shelf life — and O Buster reduces it to virtually zero.”
can also enter through packaging materials over time. The quality of the packaging is therefore critical. Although often invisible, this residual oxygen continues to affect product quality throughout storage and distribution. Oxygen exposure can cause:
• Oxidation of fats and oils
• Loss of freshness and aroma
• Texture degradation
• Colour changes
• Development of flavours
• Increased risk of mould growth
For bakery products with sensitive ingredients or extended distribution cycles, oxygen becomes a major factor limiting shelf life.
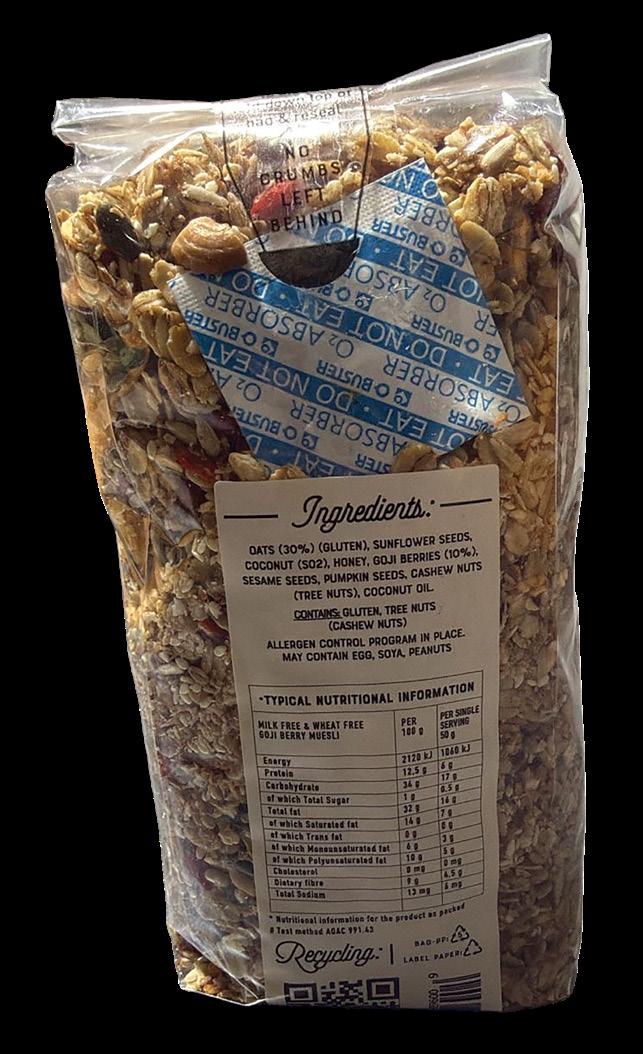
O Buster Oxygen Absorbers are small sachets placed inside sealed food packaging. Once enclosed within the pack, the absorber begins removing residual oxygen from the internal
atmosphere. The O Buster removes 99.9% of oxygen from the bag. Using a controlled oxygen-binding process, the sachet reduces oxygen levels to extremely low concentrations, creating a protective environment inside the packaging. By significantly lowering oxygen levels, O Buster helps preserve the product’s original taste, texture, appearance and overall quality throughout its intended shelf life. Unlike preservatives that are added directly into the product formulation, O Buster works as a packaging-based protection system, making it ideal for brands focused on product quality and clean-label positioning.
Gluten-free bread presents one of the most difficult shelf-life challenges in bakery manufacturing. Without gluten’s natural structural properties, these breads often become dry, crumbly or stale more quickly than conventional bread products. In addition, the moisture levels required to maintain softness can create favourable conditions for aerobic mould growth. O Buster Oxygen Absorbers help create a lowoxygen environment inside the package, reducing conditions that support spoilage while helping maintain softness, freshness and eating quality. For manufacturers supplying supermarkets or regional distribution networks, this additional shelflife protection can significantly reduce returns and product waste.
Biscuits may appear shelf-stable, but they remain highly sensitive to oxygen exposure — particularly when formulations include butter, vegetable oils, milk powders, nuts or other fat-containing ingredients. Oxidation of these fats can result in rancidity, stale flavours and aroma loss, directly impacting consumer acceptance. By removing residual oxygen from the package, O Buster helps preserve the crispness, flavour integrity and sensory quality of biscuits over extended storage periods. This makes it especially valuable for premium biscuit manufacturers, export suppliers and brands seeking longer shelf stability across multiple retail channels.
Packaged rotis require flexibility, softness and freshness to meet consumer expectations. During storage, oxygen exposure can contribute to texture deterioration, causing rotis to become dry, tough or less pliable. O Buster helps maintain product quality by minimising oxidative changes and supporting a more stable internal packaging environment. For manufacturers supplying ready-to-eat or convenience flatbread markets, this can improve product consistency throughout the supply chain.
Brownies formulated with high levels of butter, oils, nuts or other fat-rich ingredients are particularly vulnerable to oxidation. As fats react with oxygen, products may develop undesirable flavours, aroma changes and reduced freshness over time. O Buster Oxygen Absorbers help protect these rich formulations by reducing oxygen exposure, preserving both flavour and texture throughout storage. This allows manufacturers to deliver a product that maintains its indulgent eating experience for longer.
As bakery manufacturers continue to focus on quality,
consistency and market expansion, packaging technology plays an increasingly important role. O Buster Oxygen Absorbers offer a simple but highly effective way to extend shelf life in bakery and confectionery products, helping manufacturers protect product quality from production line to consumer shelf. For bakery packaging solutions, manufacturers can contact Kubepac Pty Ltd at www.kubepac.com.
Kubepac – www.kubepac.com

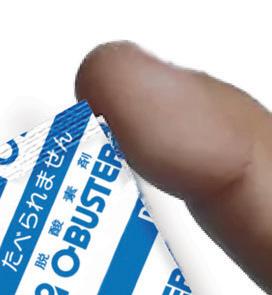
Beyond product preservation, oxygen control offers measurable commercial advantages:
• Reduced spoilage and product returns
• Improved shelf stability during distribution
• Greater confidence in export and retail supply chains
• Lower food waste
• Enhanced consumer satisfaction
• Stronger brand protection.

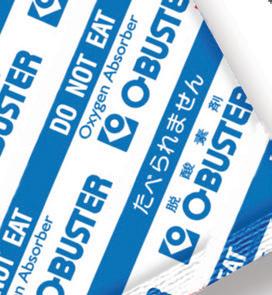





Oxygen absorbers are used to remove oxygen from within a sealed environment, creating a nitrogen environment for long-term food storage. They protect dry foods from insect damage and mould to help preserve product quality.
When used with proper packaging and sealing, the oxygen in the packaging is greatly reduced.
Oxygen Absorbers Maintain Quality, Freshness and Flavour of Food





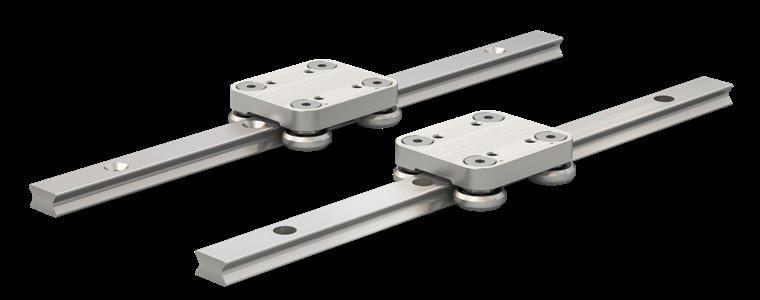
BMG supplies Rollon linear motion systems engineered for hygienic, high-performance automation across meat, poultry, fish and food processing environments.
BMG supplies and supports highspecification linear motion systems from Rollon, which are engineered for high-performance automation in many industries, including food processing, where hygiene, durability and operational continuity are essential.
“Meat, poultry and fish processing lines place unique stresses on automation components, which is why selection of the correct equipment is so critical,” says Leon Koekemoer, BMG’s Linearway & Ball Screw Product Specialist. “Rollon motion guidance systems have been developed in line with stringent industry regulations for global hygiene standards and offer advantages over conventional guides and actuators. Rollon’s advanced sealing technology, corrosion resistance and durable materials ensure extended service life, while reducing the risk of product contamination and mechanical failure. We also recommend the use of FDA-compatible lubricants to further ensure food-safety compliance.”
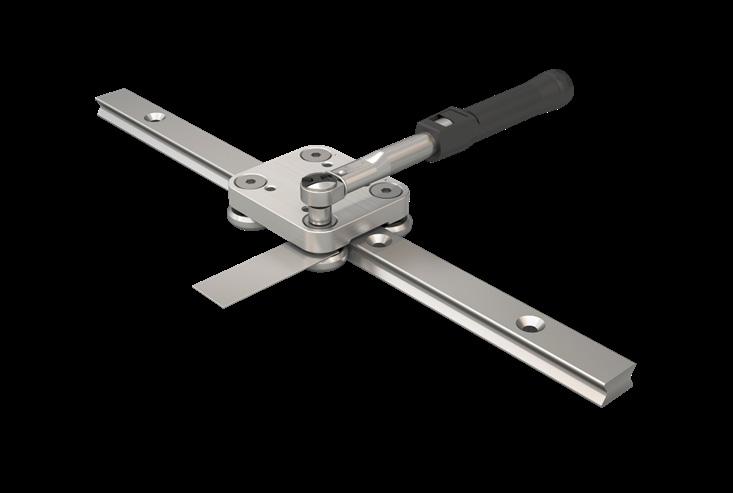
Rollon’s MiniRoller Rail and ELM actuator systems provide OEMs and integrators with solutions that endure continuous duty and aggressive sanitation, without compromising motion precision or operational reliability. These robust systems have a sealed design, with corrosion resistance and features for easy cleaning, required for continuous operation in aggressive washdown and con tamination-sensitive environments.
“Hygienic by design. Reliable by engineering.”
delivers a compact, roller-bearing linear guide system with induction-hardened raceways (58—62 HRC) and preload-adjustable stainless-steel rollers. This configuration ensures smooth, quiet travel and minimal backlash under moderate loads. Misalignment tolerance supports installation on less-than-perfect mounting surfaces, while the slider body and rollers are manufactured from stainless steel to resist rust and chemical attack. The rail itself is nickel-plated and hardened to withstand mechanical shock and caustic cleaning agents. This system, which is food-safe and hygienic, is suitable for slicing, deboning, con veying and robotic picking systems in red meat, poultry and seafood lines.
or for use in corrosive atmospheres, such as brine and blood-rich zones typical of poultry evisceration or fish gutting lines.
The ELM’s low-profile design reduces the accumulation of contaminants and enables rapid cleaning cycles. Mounting options and drive configurations can be customised, and integration into multi-axis systems is straightforward due to the profile’s modular compatibility.
The BMG team offers full engineering support, including CAD configuration, integration assistance, product selection and lifecycle optimisation services. Rollon systems are ideally suited for OEMs building hygienic conveyors, portioners, sorters, cutters and handling systems across food protein processing environments.
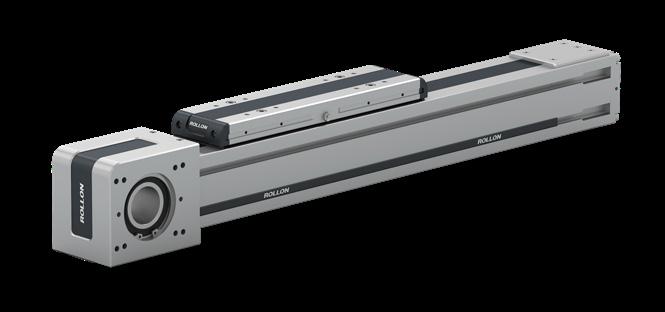
For linear actuator applications in food processing, specialists recommend the Rollon ELM series, which offers a sealed belt-drive solution with internal recirculating ball guides housed in an extruded aluminium profile. A polyurethane sealing strip shields internal components from high-pressure washdowns and airborne contaminants. To enhance sealing performance, the unit can be positively or negatively pressurised (typically 0.7—0.8 bar). An anti-corrosion version with stainless-steel components is available for applications with direct fluid exposure
BMG’s Rollon portfolio includes linear guides, telescopic rails, actuators and multiaxis systems, as well as ball screws and rotational units — engineered to function reliably in heavy-duty industrial operations. These robust components withstand high loads, continuous use and exposure to harsh environments, making them suitable for other sectors including automotive assembly, electronics manufacturing, packaging and materials handling.
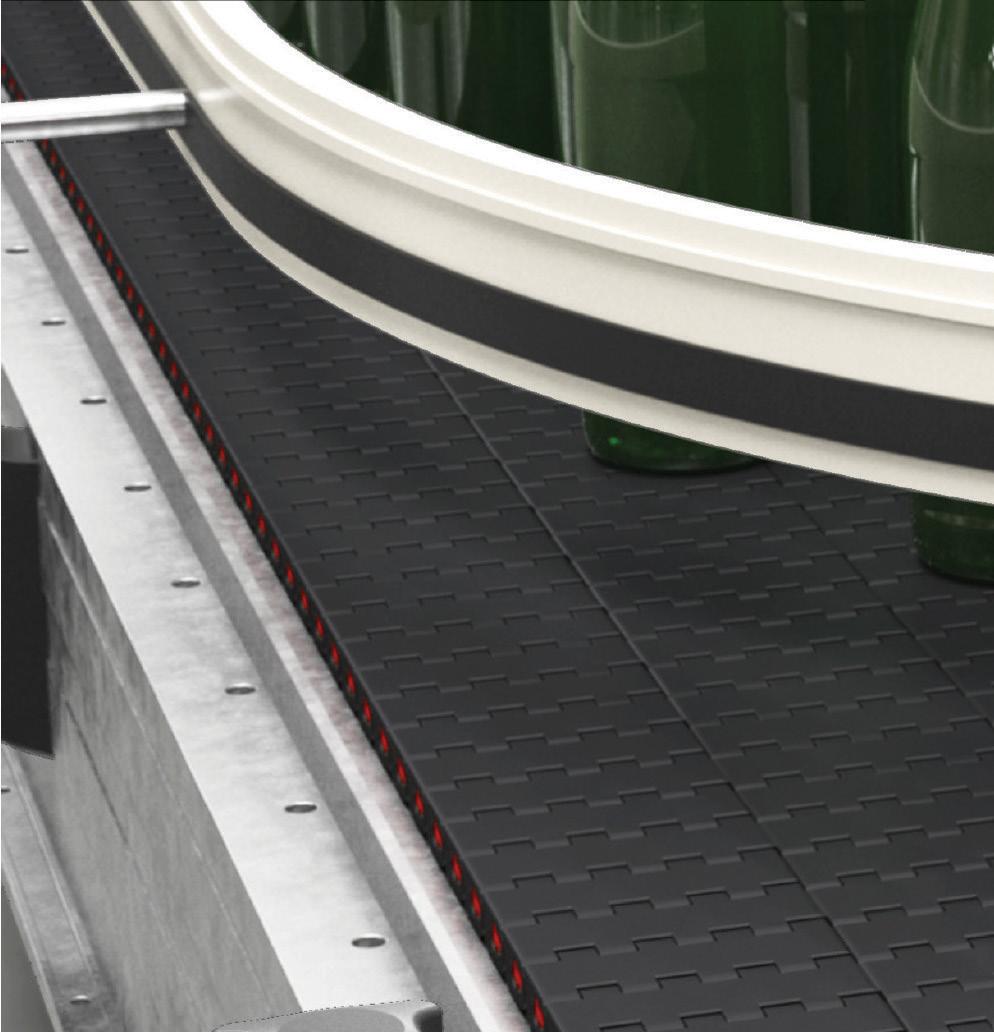
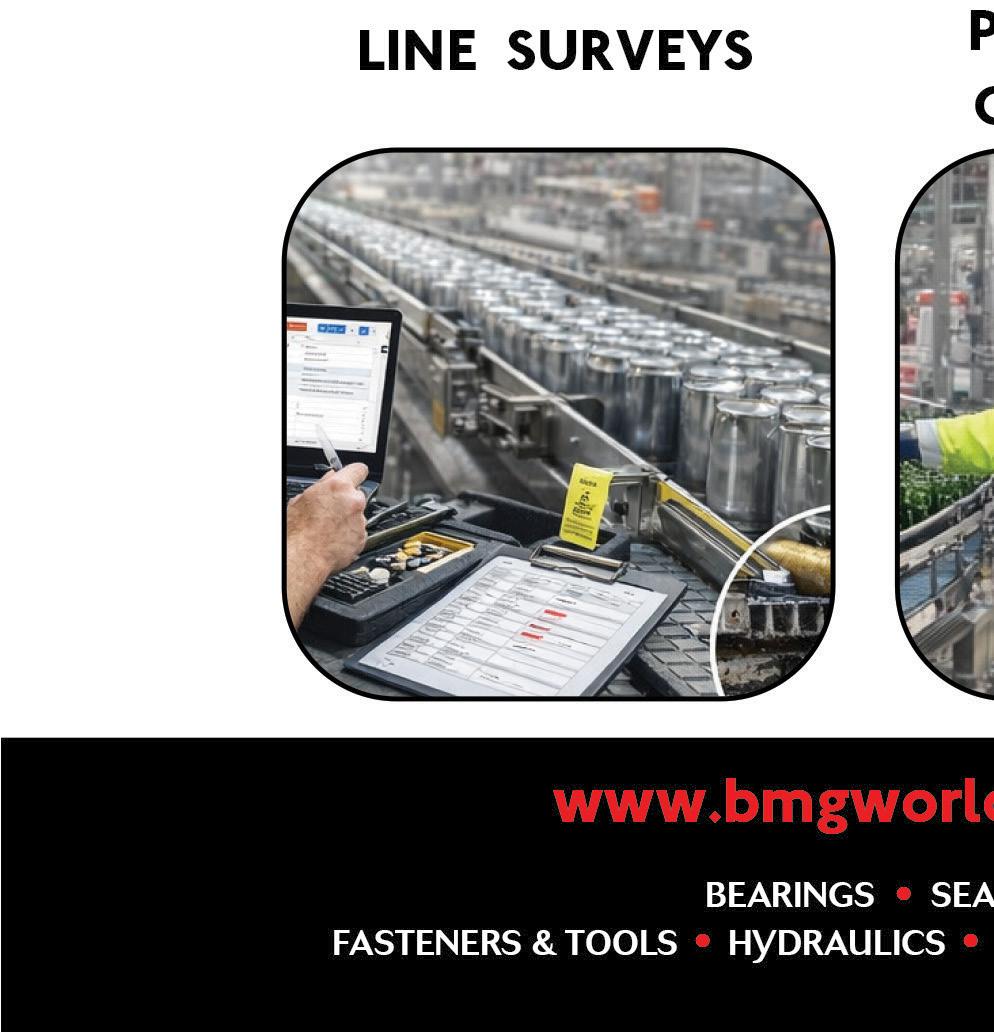
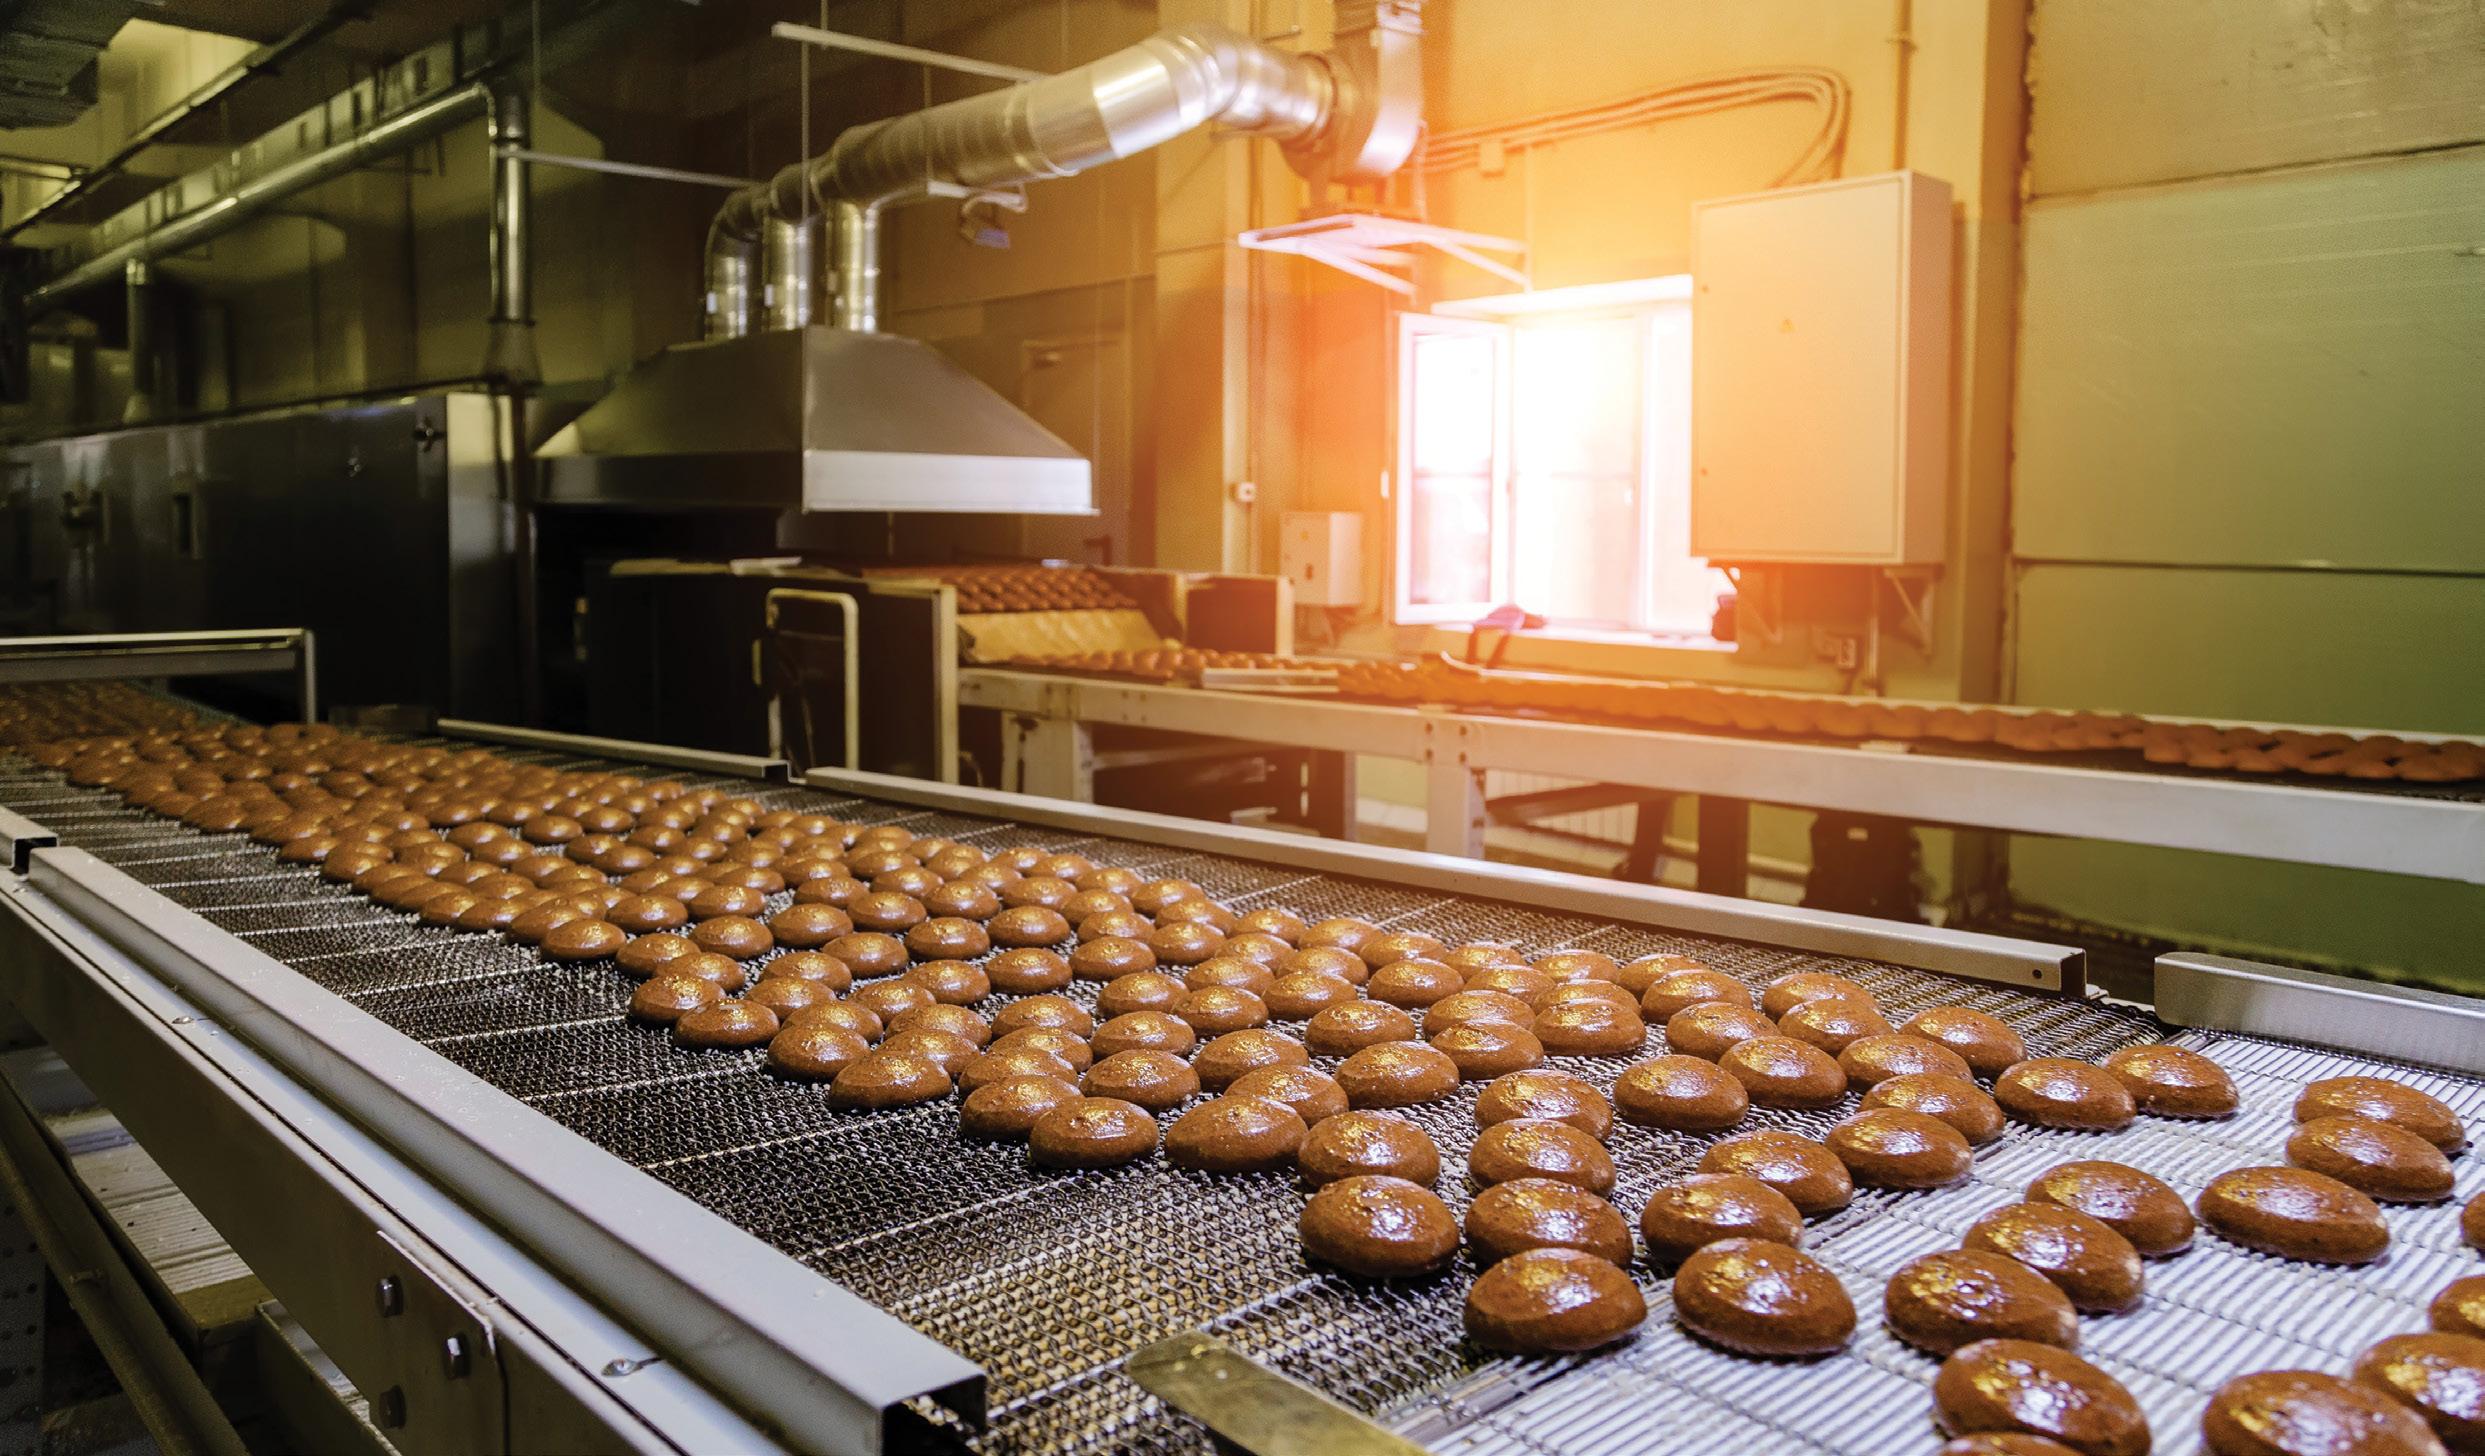
Tegman supplies wire conveyor belting solutions across Southern Africa, keeping food, mining and industrial operations running reliably every day.
In today’s competitive industrial environment, efficiency, reliability and productivity are essential to maintaining a successful operation. Whether products are being processed, coated, heated, cooled, frozen or transported, conveyor systems remain a critical part of the manufacturing process. At the heart of these systems is the conveyor belt — a component that directly impacts production performance, product quality and operational uptime.
Tegman has established itself as a trusted supplier of high-quality wire conveyor belting solutions, serving a diverse range of industries across Southern Africa. Through a combination of technical expertise, industry knowledge and a commitment to customer service, Tegman provides conveyor solutions designed to meet the unique challenges faced by modern manufacturers and processors.
Wire conveyor belts offer significant advantages over many alternative conveying solutions. Their strength, durability, temperature resistance and open construction make them suitable for a wide variety of applications where reliability and performance are essential. From food processing facilities and packaging plants to heat treatment operations, automotive manufacturers, tool makers and mining operations, wire conveyor belting continues to play a vital role in industrial production.
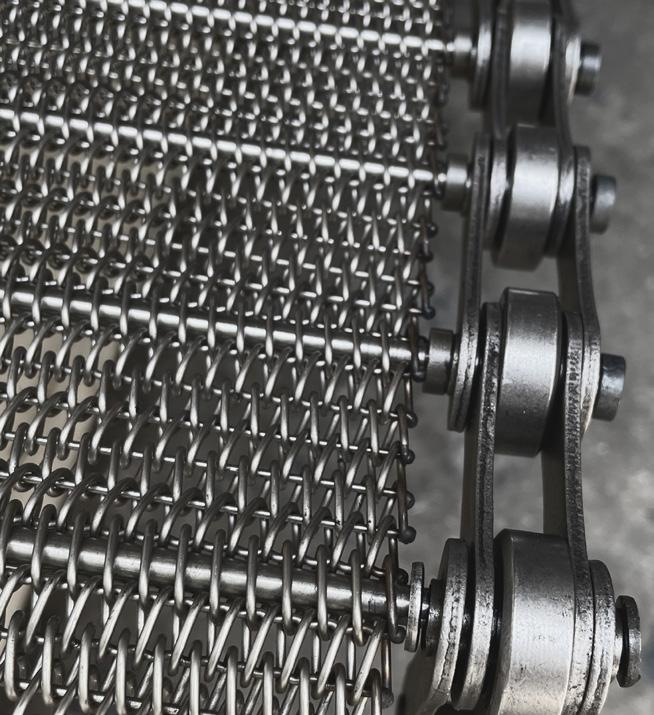
One of the most widely used wire belting solutions supplied by Tegman is the balanced weave conveyor belt. Known for its versatility and dependable performance, the balanced weave design provides excellent product support while allowing airflow, drainage and heat transfer where required. These characteristics make it suitable for applications ranging from processing and packaging to cooling and drying operations.
Honeycomb conveyor belts are another popular solution within Tegman’s product offering. Designed for strength and durability, honeycomb belts provide excellent load-carrying capability while maintaining an open structure that promotes airflow and efficient processing. These belts are commonly used in industries where products are exposed to heating, cooling, drying, washing or freezing processes and where long service life is a priority.
Ladder belts, often referred to as enrober belts, are widely recognised for their effectiveness in coating and finishing applications. Their open design allows excess material to pass through the belt while maintaining smooth and consistent product movement. While commonly associated with confectionery and bakery operations, ladder belts are also used in a variety of industrial applications where efficient product handling and airflow are important.
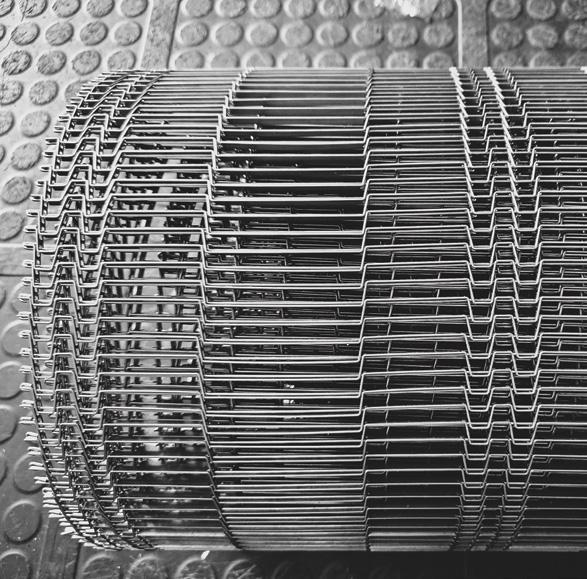
Spiral freezer belts form an important part of Tegman’s wire belting
portfolio. Designed to operate in demanding low-temperature environments, these belts help manufacturers maximise airflow while maintaining product stability and efficient throughput. Their robust construction and reliable performance make them a preferred solution for freezing applications where consistency and productivity are critical.
Beyond the food industry, Tegman’s wire conveyor solutions support a broad range of industrial sectors. In heat treatment facilities, conveyor belts are required to withstand extreme temperatures while maintaining their structural integrity and operational performance. Applications such as hardening, tempering, annealing and stress relieving demand conveyor solutions that can perform continuously under challenging conditions. Tegman’s wire belts are designed to meet these requirements, helping customers maintain production efficiency and product quality.
Tool manufacturing operations also rely heavily on dependable conveyor systems. Components often pass through multiple stages of production, including heat treatment, washing, drying, inspection and finishing. Conveyor reliability is essential to maintaining throughput and ensuring consistent product quality. Tegman’s experience in these applications allows customers to select the most suitable belt for their specific production requirements.
In the automotive and engineering industries, wire conveyor belts are used in a variety of manufacturing processes, including component cleaning, drying, coating, curing and assembly operations. These environments re-
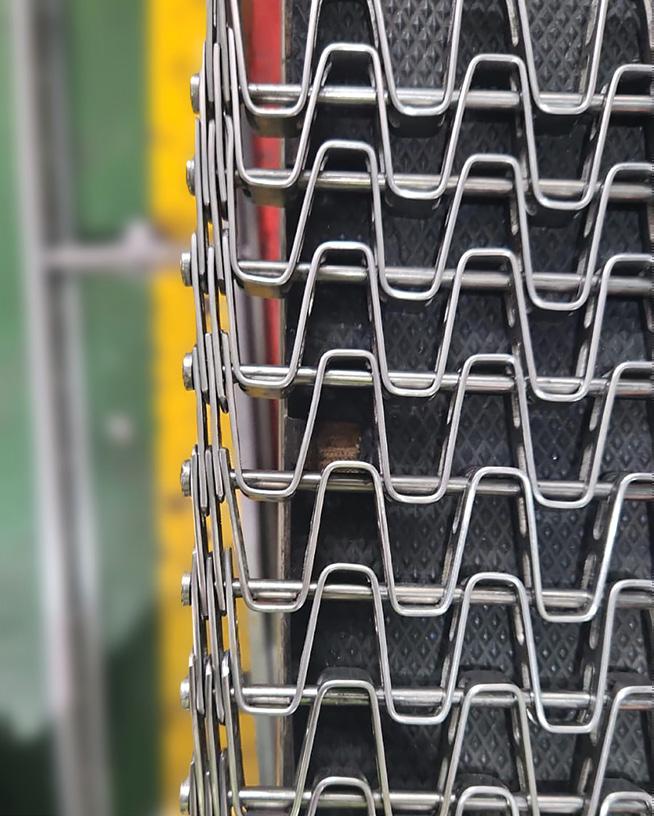
Spiral freezer belts — one of Tegman’s key product offerings — are specifically engineered to maximise airflow in demanding lowtemperature environments, helping food manufacturers maintain product stability and consistent throughput even under the most challenging freezing conditions.
“Tegman remains committed to supporting customers with highquality wire belting solutions designed to perform across a diverse range of industries and applications — keeping businesses moving forward.”
quire conveyor solutions capable of delivering reliable performance while reducing maintenance requirements and minimising downtime. Powder coating and surface finishing operations represent another important application for wire conveyor belting. Products moving through cleaning, coating, curing and finishing stages require stable and dependable conveying systems. The open construction of wire belts allows for effective airflow and heat transfer, contributing to improved process efficiency and product consistency.
Mining, recycling and heavy industrial sectors also benefit from the durability and strength of wire conveyor belts. These industries often operate in harsh environments where equipment is subjected to abrasive materials and demanding operating conditions. Tegman’s wire belting solutions are selected to provide long-term reliability and dependable performance in these challenging applications.
At Tegman, the focus extends beyond simply supplying conveyor belts. The company works closely with customers to understand their production requirements, operational challenges and performance objectives. By combining product knowledge with practical industry experience, Tegman assists customers in identifying solutions that improve
efficiency, reduce downtime and maximise return on investment.
As industries continue to pursue greater productivity and operational excellence, the demand for reliable conveyor solutions continues to grow. Tegman remains committed to supporting customers with high-quality wire belting solutions designed to perform across a diverse range of industries and applications. From balanced weave belts and honeycomb belts to ladder belts, spiral freezer belts and specialised wire mesh solutions, Tegman continues to deliver conveyor technology that keeps businesses moving forward.
Balanced weave belt: Versatile all-rounder with excellent product support; allows airflow, drainage and heat transfer. Ideal for processing, packaging, cooling and drying.
Honeycomb belt: High load-carrying capacity with open structure for efficient airflow. Used in heating, cooling, drying, washing and freezing processes. Ladder belt (Enrober belt): Open design allows excess coating material to fall away while maintaining smooth product movement. Widely used in confectionery, bakery and industrial finishing.
Spiral freezer belt: Robust construction for demanding low-temperature environments. Maximises airflow and maintains product stability and throughput in freezing applications. Specialised wire mesh: Custom wire mesh solutions for mining, recycling, heat treatment, automotive, powder coating and heavy industrial sectors.
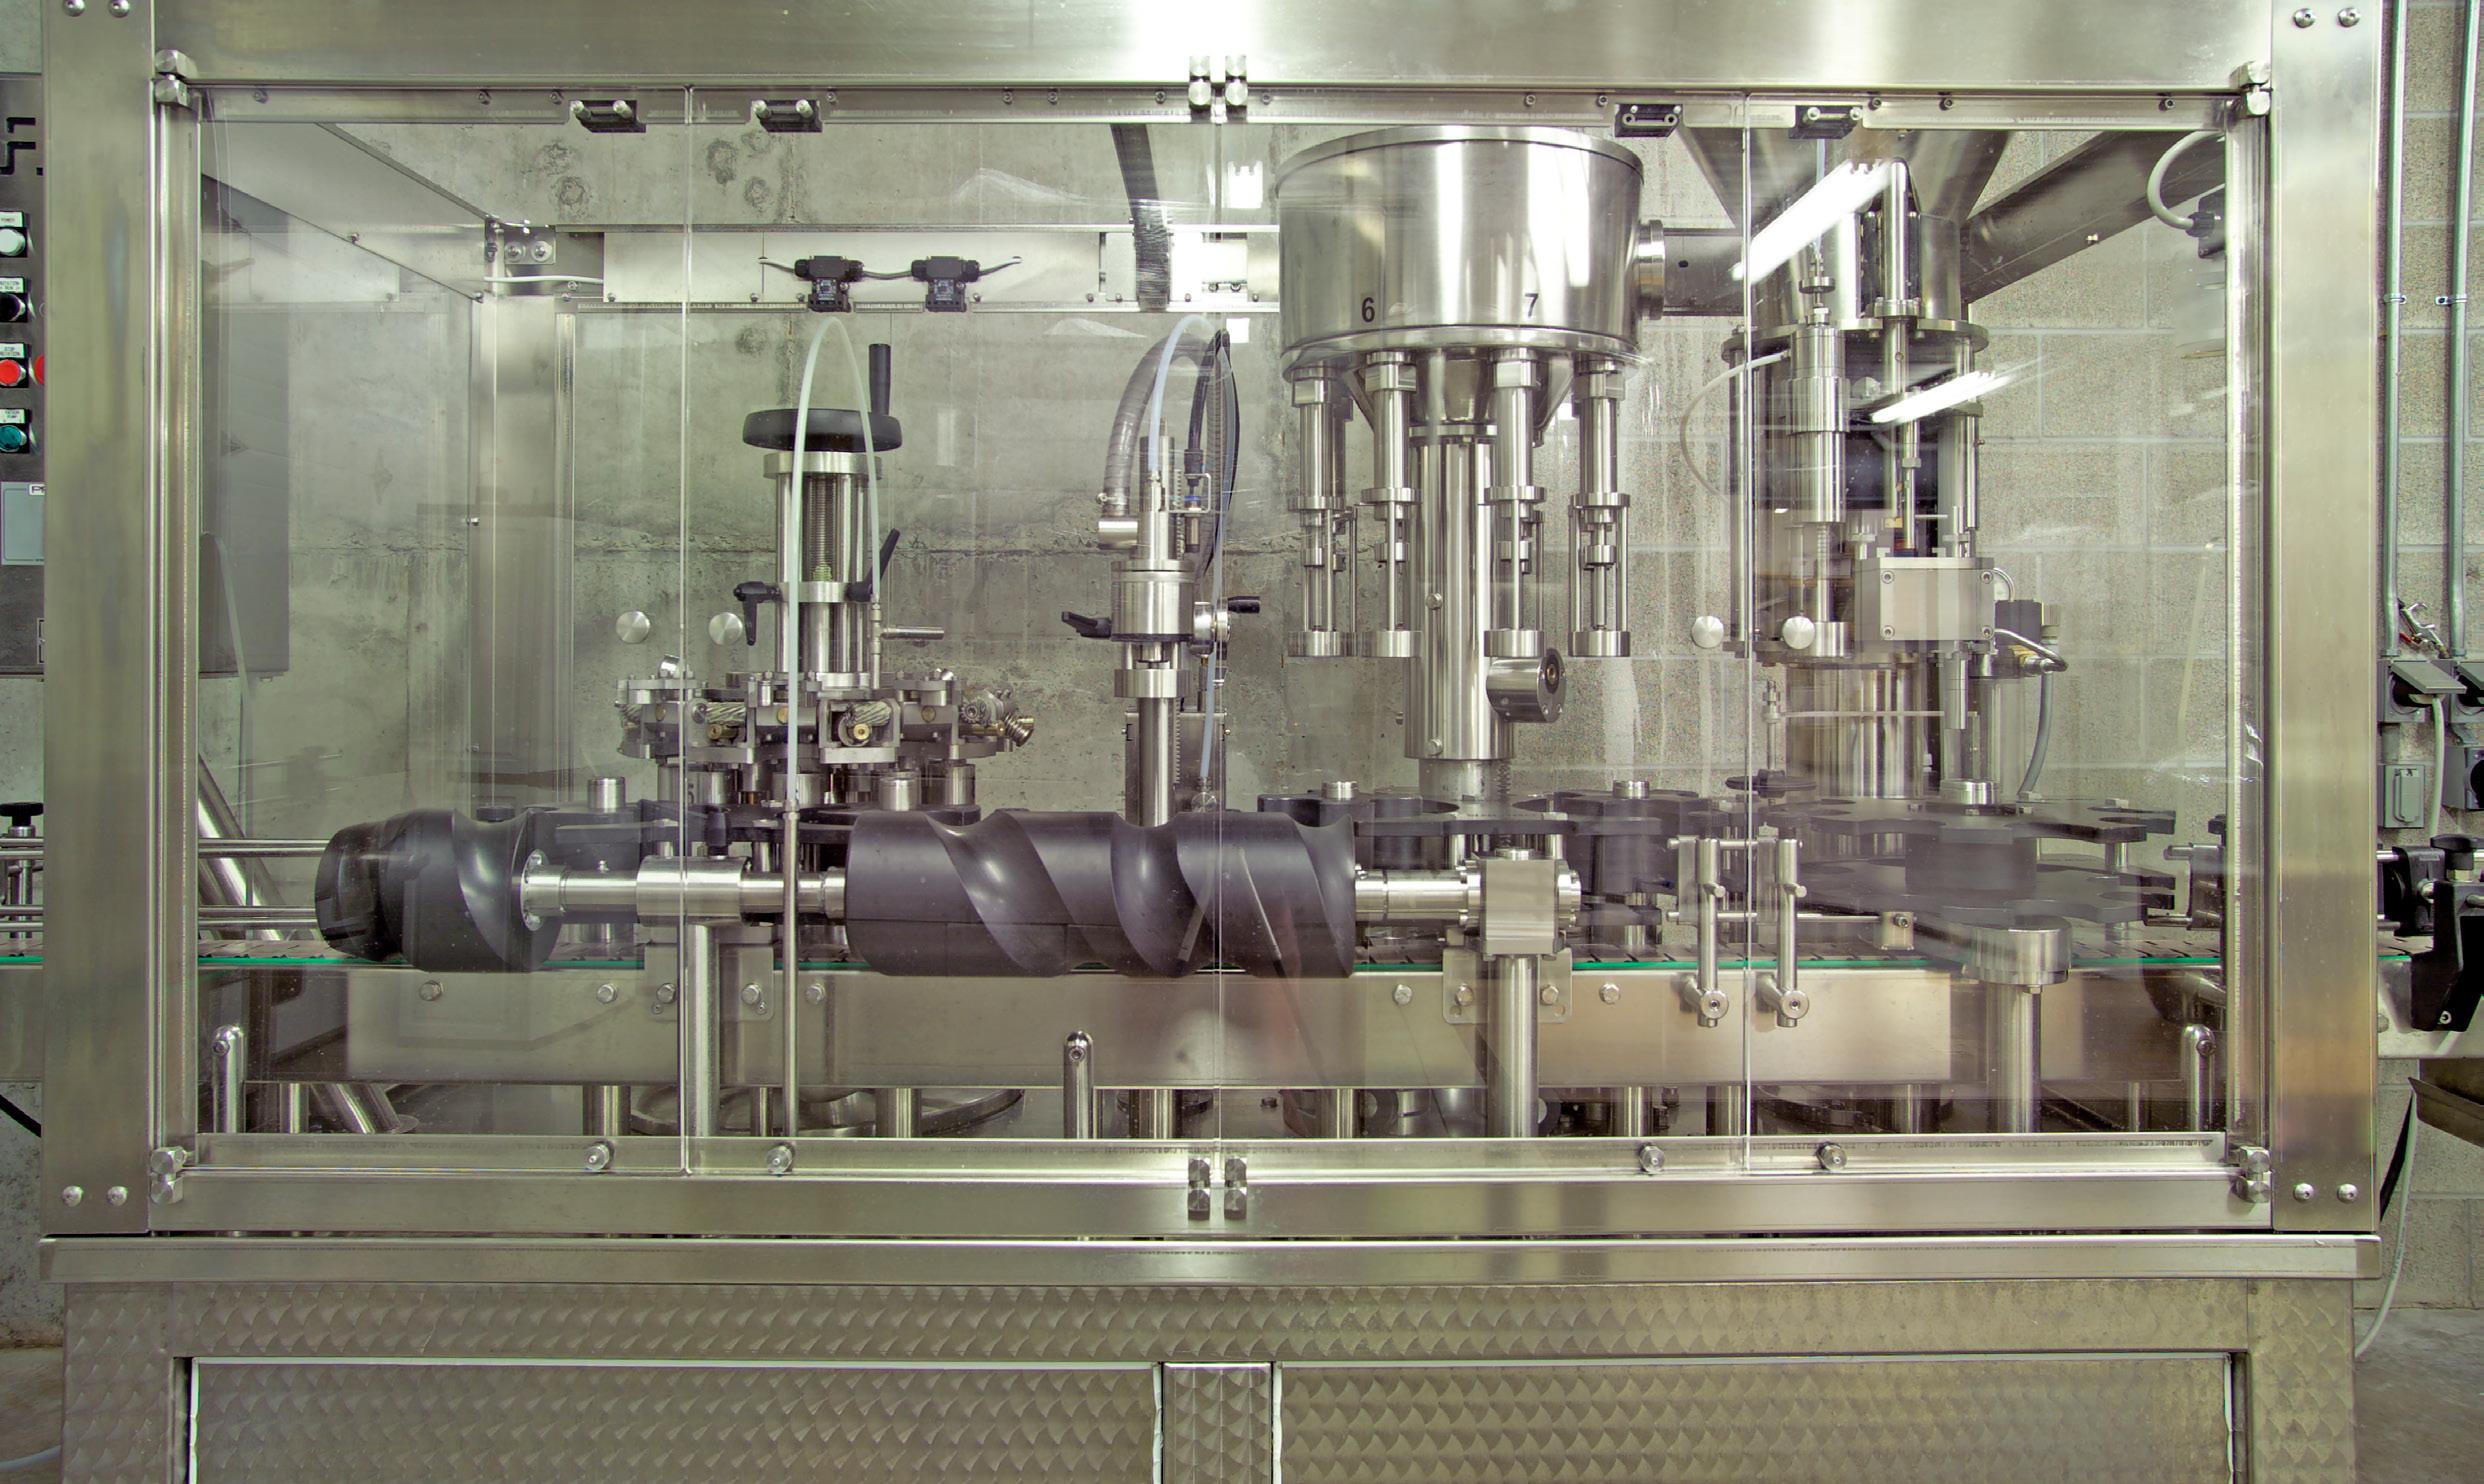
At IJP Filling & Labelling, we bring over 30 years of proven expertise in the packaging and automation industry.
As a trusted South African manufacturer, we specialise in the design, engineering, and installation of advanced filling, capping, labelling, and conveyor systems all built for maximum efficiency, precision, and reliability in your production line.
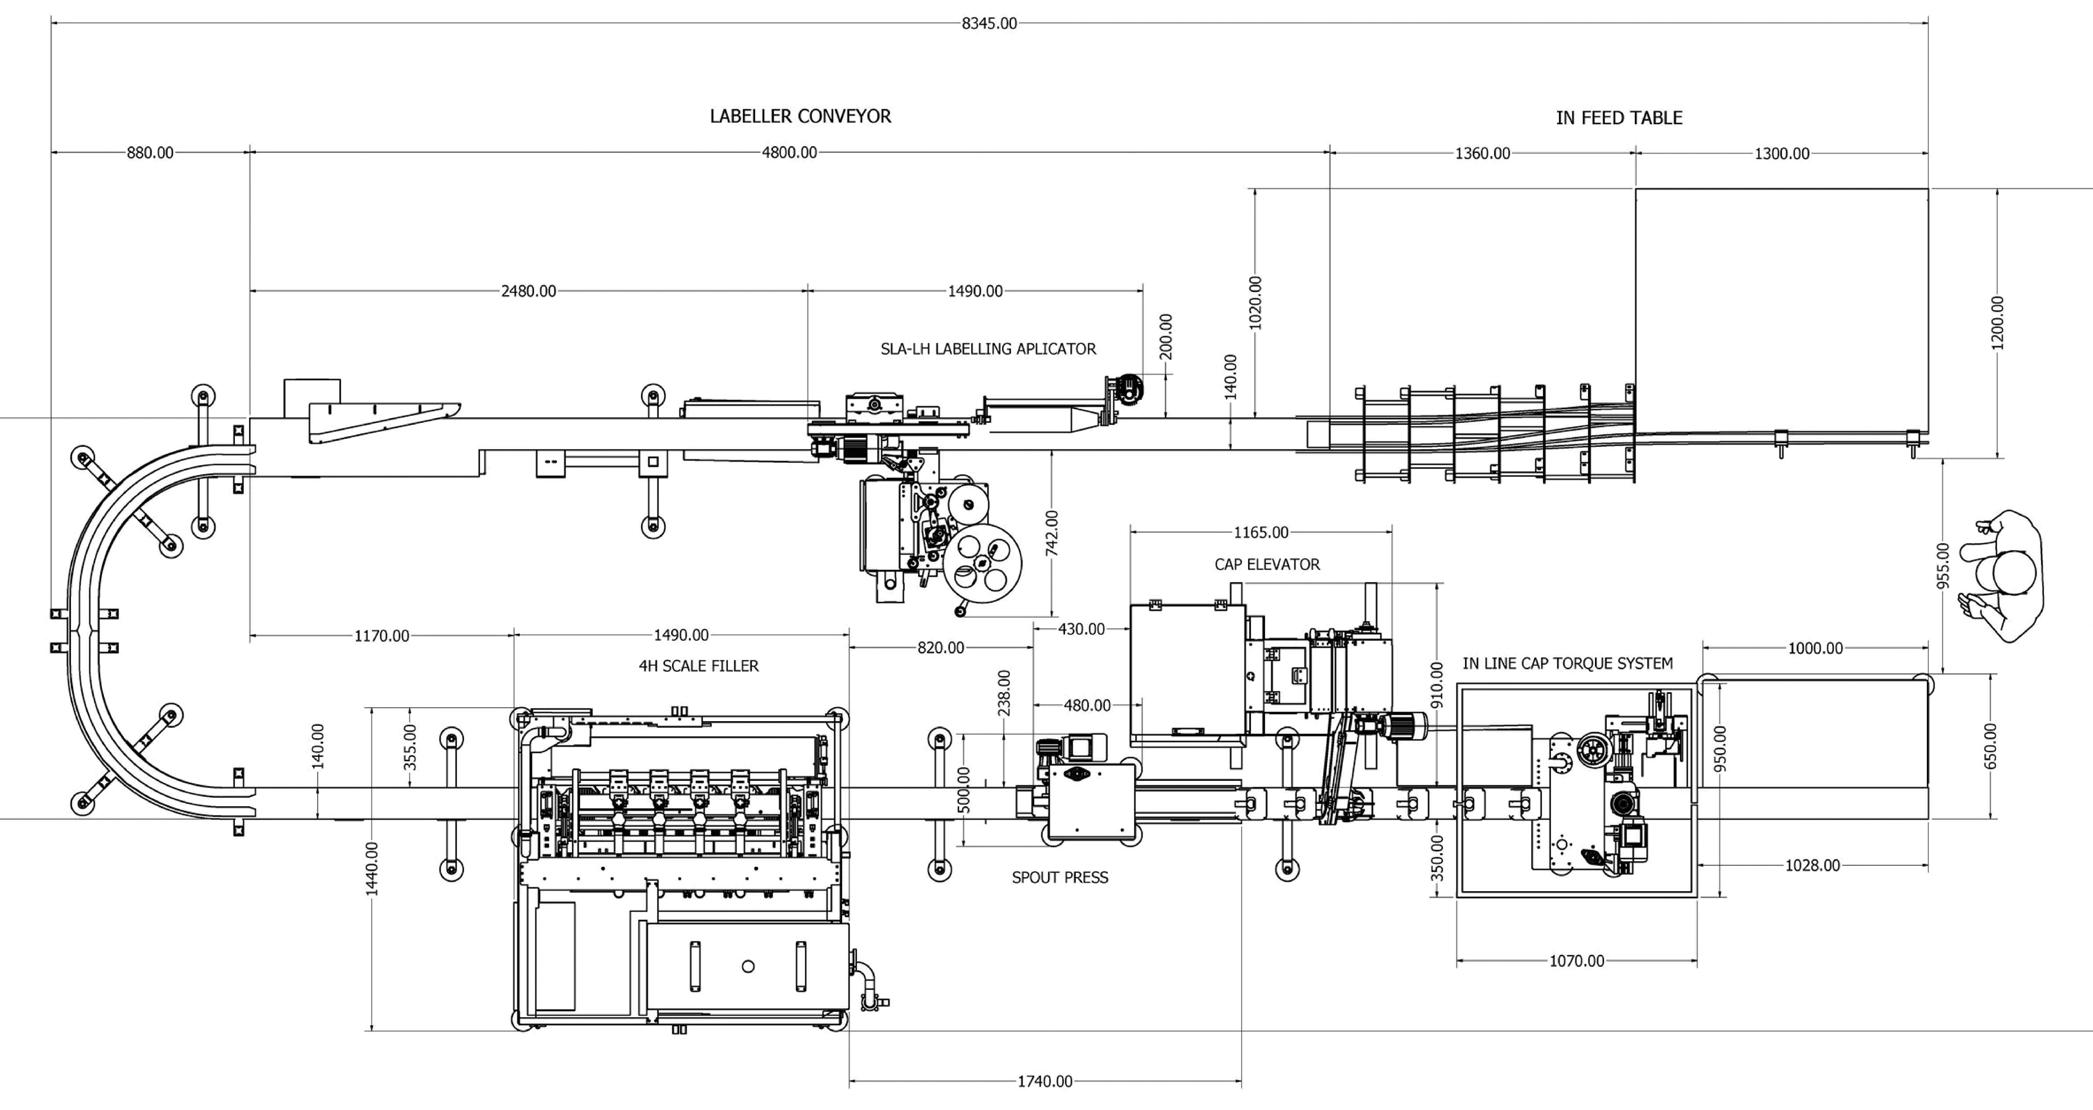
Our dedicated technical team partners closely with system integrators, equipment suppliers, and component manufacturers to deliver custom-engineered packaging automation solutions that perfectly match your business requirements. From small-scale production setups to large industrial manufacturing environments, IJP ensures seamless integration and optimized performance at every stage of the process.
We take pride in helping clients streamline operations, minimise downtime, and boost productivity through intelligent system design and top-tier engineering. Whether you’re launching a new production facility or upgrading an existing line, our experts provide comprehensive factory layout planning and workflow optimisation to ensure smooth, continuous operation.
At IJP, we don’t just build machines we
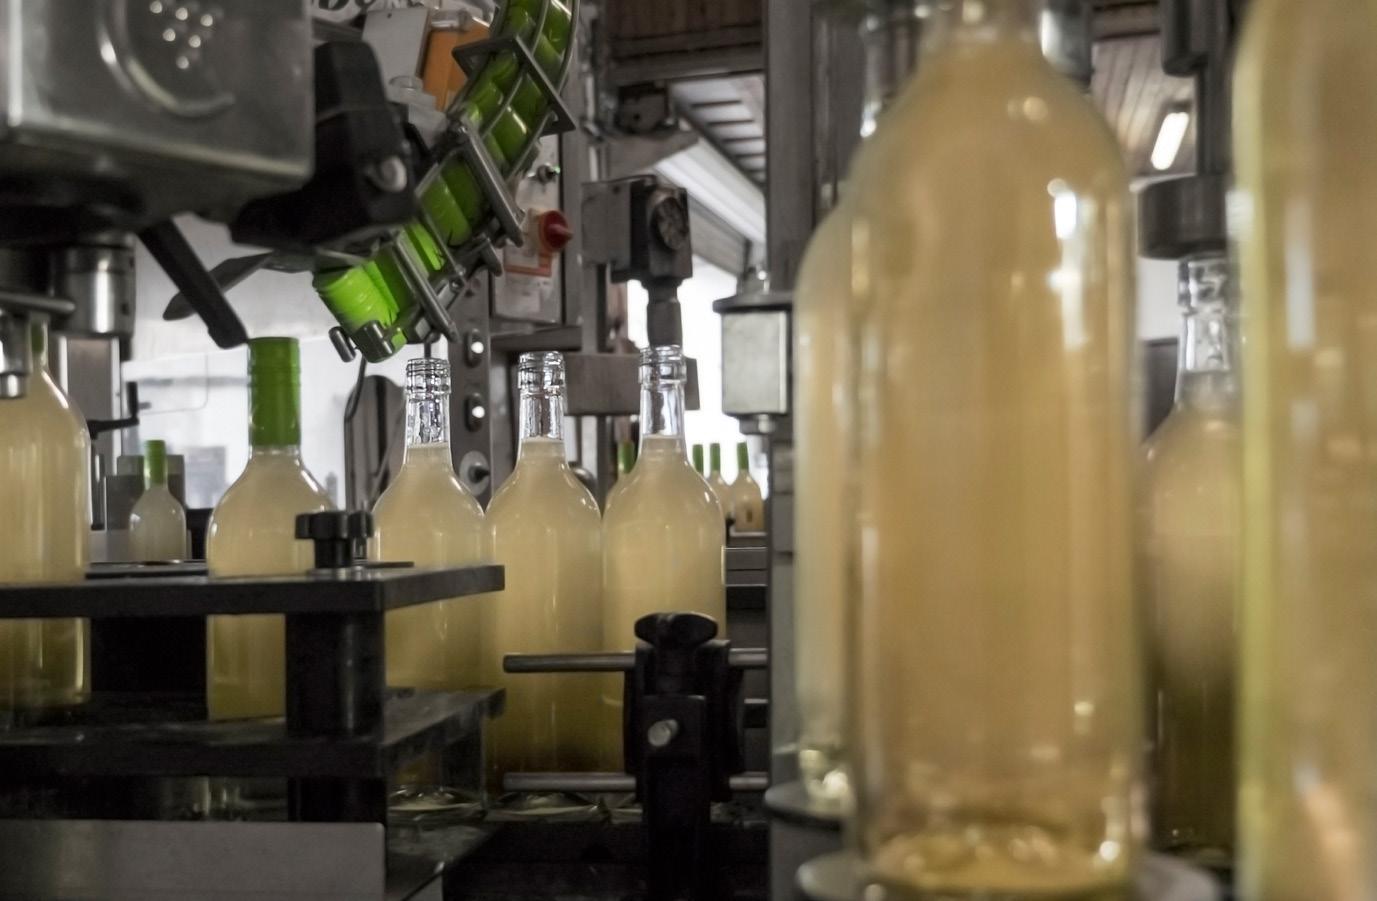
build long-term partnerships. Our commitment to innovation, quality craftsmanship, and exceptional after-sales service ensures that every client benefits from reliable performance, reduced maintenance costs, and measurable ROI.
With an expanding range of automated packaging machinery tailored for industries such as food and beverage, pharmaceuticals, chemicals, and manufacturing, IJP Filling & Labelling continues to set the benchmark for excellence in South African packaging solutions.
We specialise in custom machine design and engineering solutions created to meet the unique requirements of your packaging and production operations. With over 30 years of industry experience, our team combines innovation, precision, and practical expertise to design filling, capping, labelling, and conveyor systems that deliver unmatched performance and efficiency.
Our custom design process begins with understanding your production goals, product specifications, and workflow chal-
lenges. Whether you require a specialised low-viscosity filling line, a high-viscosity paste filler, a carbonated beverage system, or a fully integrated packaging conveyor solution, we engineer machines that fit seamlessly into your existing setup. Each design is optimised for durability, precision, and ease of operation, ensuring consistent performance even under demanding industrial conditions.
IJP’s in-house design team utilises advanced CAD modelling and 3D simulation to develop customised machinery that maximises productivity while maintaining the highest standards of quality and hygiene. From semi-automatic labelling systems for small production runs to fully automated highspeed lines, we design every machine to align perfectly with your brand’s requirements and operational scale.
Our custom-built solutions also prioritise user-friendliness, low maintenance, and adaptability, allowing for quick product changeovers and reduced downtime. Each system is backed by our ongoing technical support, ensuring your investment remains efficient and reliable over time.
Partner with IJP Filling & Labelling for a tailor-made packaging solution that enhances your production efficiency, reduces waste, and supports long-term growth. No matter your industry, food and beverage, cosmetics, pharmaceuticals, or manufacturing we design machines that perform beyond expectations.
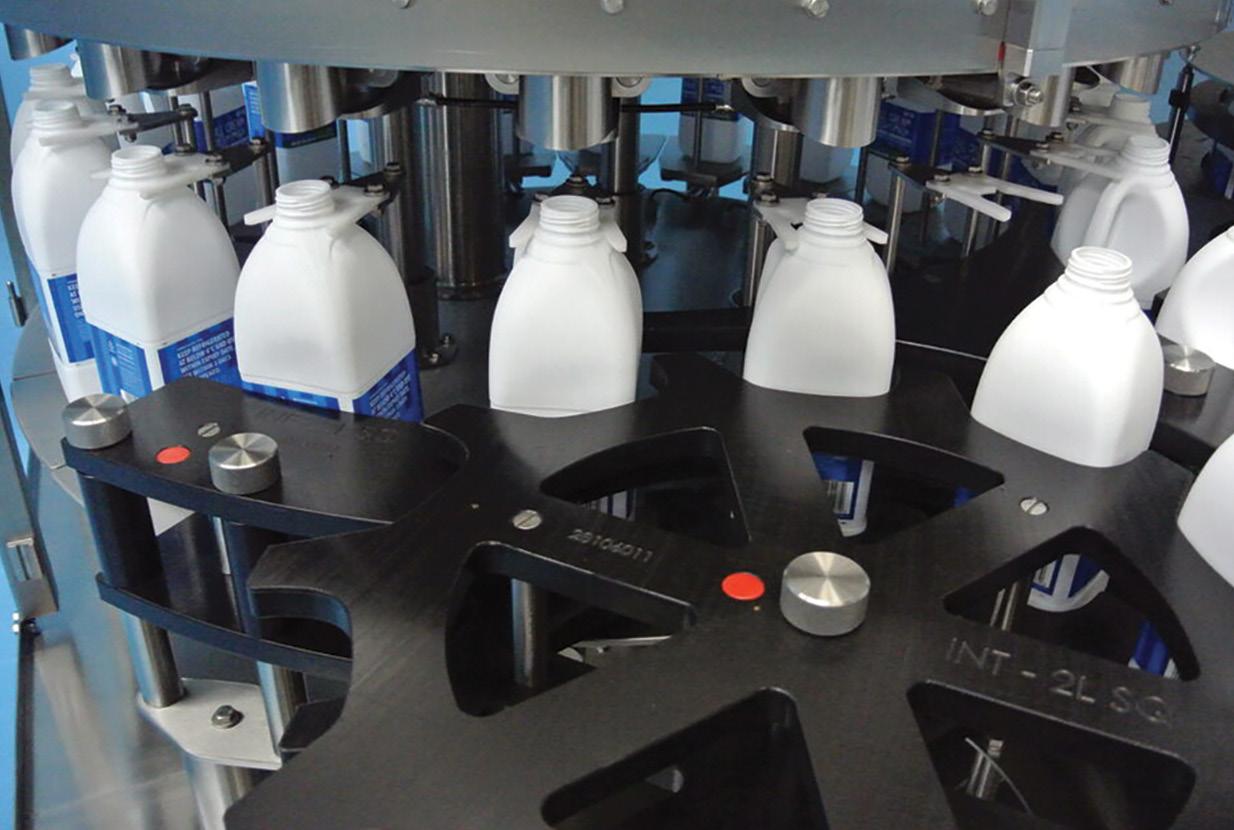
1. Filling products: IJP Filling & Labelling provides high-performance filling machines designed for precision, consistency, and efficiency in industrial production. Our advanced filling systems handle liquids, pastes, and viscous products with accuracy, minimising waste and maximising productivity. Trusted across South Africa, we deliver reliable, innovative filling solutions for diverse packaging needs.
2. Labelling: IJP Filling & Labelling offers advanced labelling machines engineered for precision, speed, and reliability. Our systems provide accurate label placement on various container types and sizes, enhancing product presentation, reducing downtime, and streamlining packaging operations across diverse industries in South Africa.
3. Capping rate per hour: The company provides high-quality capping machines designed for speed, accuracy, and consistent torque control. Our systems ensure secure, reliable sealing for a wide range of container types, enhancing production efficiency, reducing product waste, and supporting seamless operations across industrial packaging lines.
4. Conveyor types: IJP Filling & Labelling offers durable and efficient conveyor systems designed to optimise material handling and production flow. Our conveyors accommodate a variety of products and environments, ensuring smooth, reliable transport, minimising downtime, and enhancing overall efficiency across industrial packaging and manufacturing lines.
In the fast-paced world of beverage production, conveyor systems operate under constant pressure. Here’s why proper conveyor lubrication is crucial for maintaining efficiency, safety, and longevity of your production lines.
In the fast-paced world of beverage production maintaining a clean, efficient and reliable conveyor system is crucial for meeting demands and ensuring smooth operations, conveyor lubrication plays a pivotal role in achieving this by reducing friction, preventing wear and tear, and extending the lifespan of conveyors. Conveyors are the backbone of beverage production lines, transporting bottles, cans, and packaging materials from one stage of the production process to another. These systems are subjected to continuous motion, high speed operations, and various environmental factors. Without effective lubrication, the friction generated during these processes can lead to increased energy consumption, bottle scuffing, breakages, down time due to maintenance and even equipment failure. One of the primary benefits of conveyor lubrication is the reduction of friction between bottles and cans, and conveyor itself. This results in decreased energy consumption, contributing to overall energy efficiency in the plant. Energy–efficient operations not only align with sustainability goals, but also lead to cost savings, making lubrication systems a valuable investment. Moreover, conveyor lubrication plays a crucial role in preventing wear and tear on conveyor components. The constant movements of materials and the exposure to contaminants can accelerate the deterioration of belts, chains and rollers. Lubrication acts as a protective barrier, minimising the impact of friction
and extending the lifespan of these components. This reduces the frequency of maintenance interventions and enhances the conveyor system’s overall reliability. Selecting the right lubricant is paramount in ensuring the effectiveness of a conveyor lubrication system. Early lubes were all soap based and had certain inherent problems. They were very sensitive to water hardness, often produced excessive foam and supported the development of microbial slimes.
Today, most lubes are based on synthetic organic compounds. They have high tolerance for water hardness, eliminating the need for water softeners. This brings cost savings by obviating the cost of running and maintaining softeners. Synthetic lubes generally do not support microbial growth on the conveyors and some formulations are antimicrobial and do not allow any bacterial or fungal slimes to form and build up on the conveyors. The floor under the conveyors is therefore
clean and slime free, which contributes to personal safety and plant hygiene.
Another positive feature of synthetic lubes is that conveyor spray nozzle blockages are greatly reduced or eliminated entirely, which saves manpower for the time to unblock the nozzles and reduce conveyor wear. Various factors, such as the type of conveyor, operating conditions, and the type of beverage being processed influence the choice of lubricant. Implementing an effective lubrication strategy involves more than just applying lubricant to moving parts. Regular inspections, monitoring systems, and proper maintenance schedules are essential elements of a comprehensive approach. In addition to the mechanical benefits, proper conveyor lubrication contributes to a cleaner and safer working environment. Over–lubrication can lead to spillage, creating slippery surfaces that pose safety hazards for plant workers. A wellmaintained lubrication system minimises the risk of spills, contributing to a safer workplace and reducing the potential for accidents and contributing to efficiency and longevity of conveyor systems.
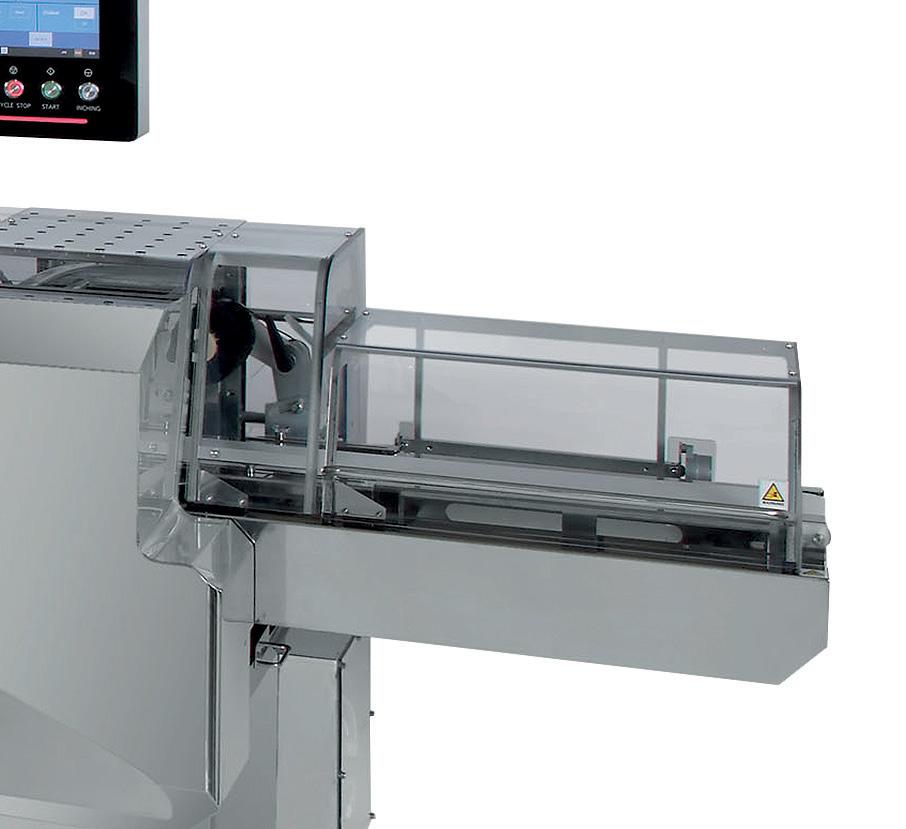
Fuji offers box-motion and rotary-motion packaging machines. These can be fully integrated with automatic infeed systems. Rotary processes deliver ultra-high-speed wrapping and sealing, while box-motion processes supply hermetic sealing.
Fuji packaging machinery anticipates customer requirements. Internal software systems on both box and rotary machines automatically calculate the size, wrapping parameters and packaging speeds from supplied information.
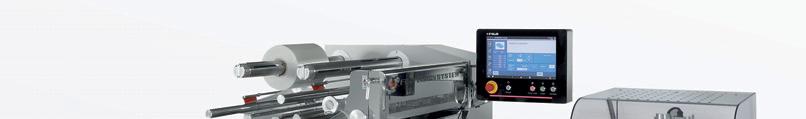
Fuji machinery is renowned for reliability and durability. Robust designs, strong sealing technology and consistent high performance make it a stable, long-term choice for many industries.
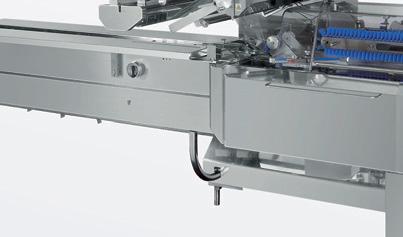
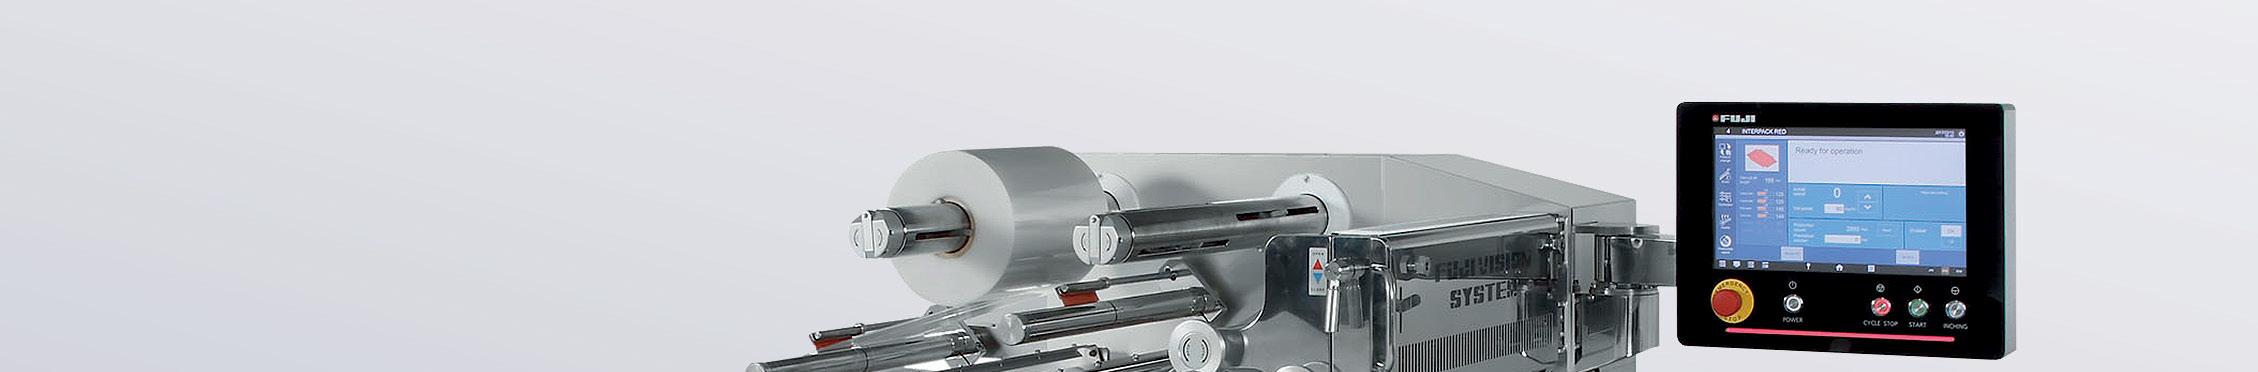
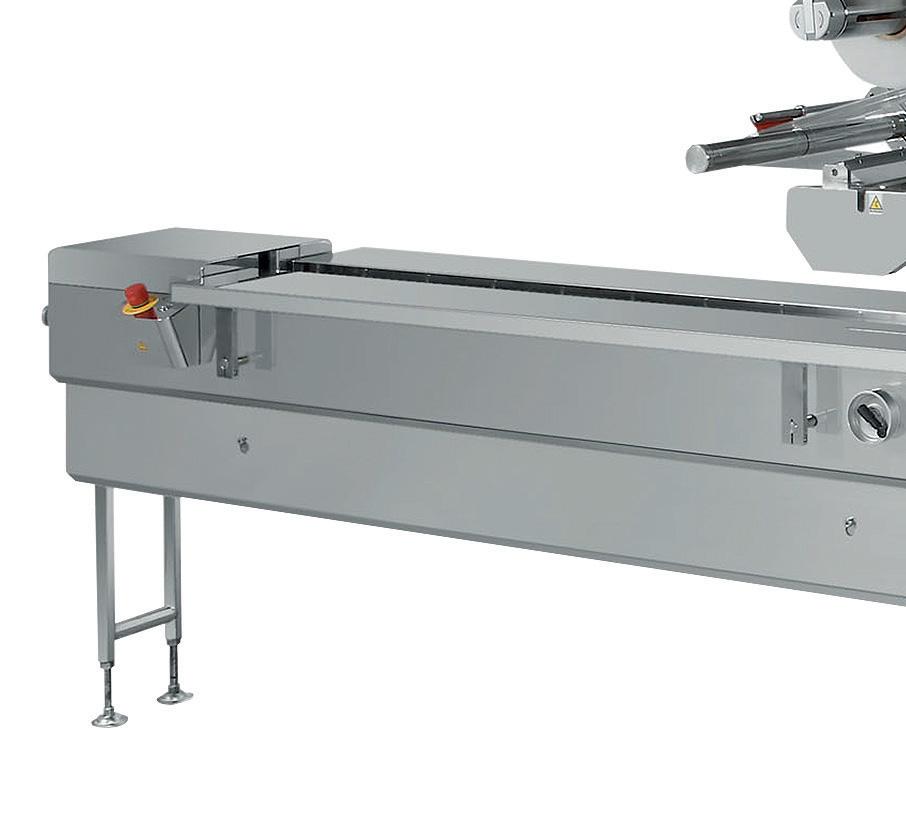

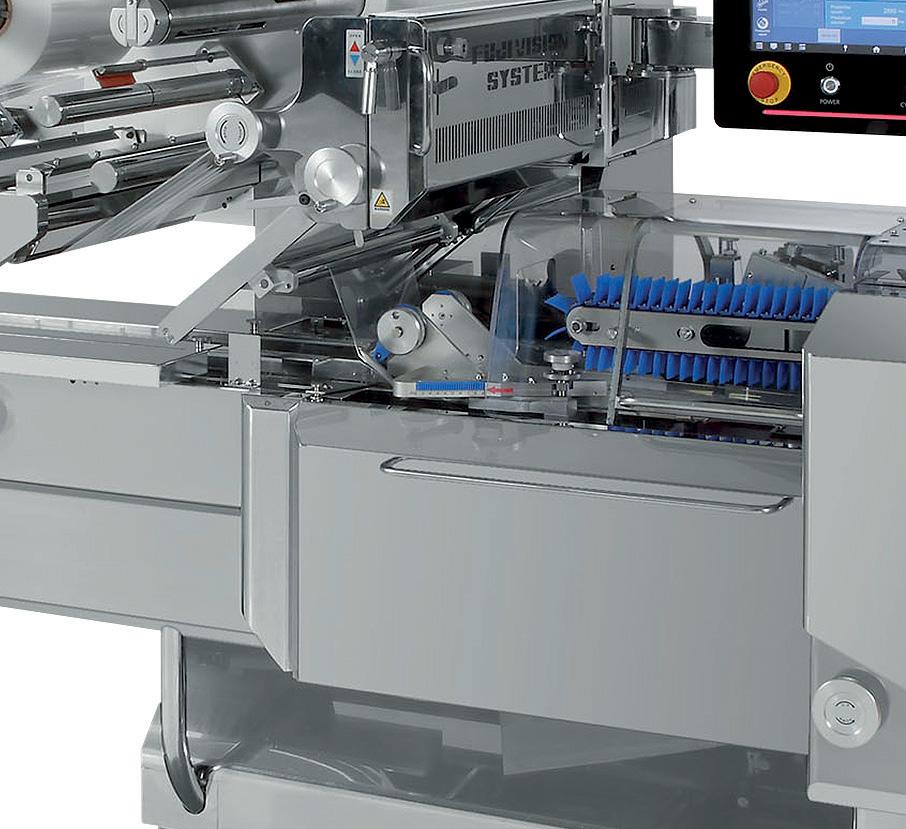
Fuji offers exible solutions that support the use of environmentally friendly mono and paper lm.
Progetto International manufacturers and distributors of automated machinery for the packaging, labelling, and filling industries. They commit themselves to fulfilling the client’s requirements, from conceptual design to implementation, delivery and after sales service. Food Review editor, Kelebogile Nondzaba, speaks to Progetto International about their latest product and service offerings.
Progetto international is one of South Africa’s leading packaging systems design and manufacturing companies. They manufacture and distribute machinery for the packaging, labelling, and filling industries and provide the best solution and equipment at a competitive price to their clients. Progetto International is recognised for its high standard of service, quality and competitive pricing, workmanship, and technology. Combining its own manufacturing of engineered designs through a team of highly skilled mechanical and electrical engineers with their approved and reliable suppliers. They commit to fill the clients’ requirements, from conceptional design to implementation, delivery and after sales service.
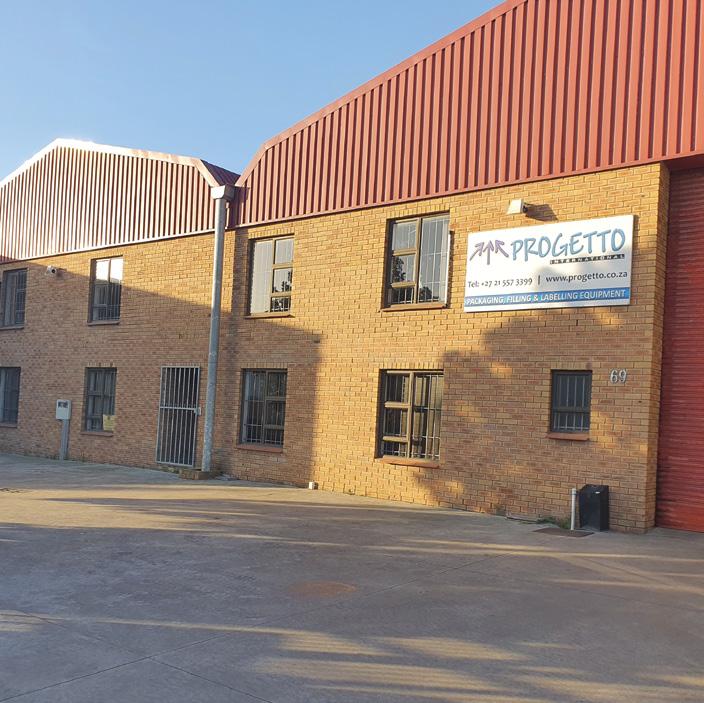
The new factory and location in Killarney gardens form their next step in the journey to expansion. With the growth of the company, logistical and capacity challenges they were obliged to seek for a larger premisses. Progetto Int was established in 2008 and its manufacturing facility is currently situated in Killarney Gardens, located in the proximity of Cape Town. The aim is to provide the best solutions and equipment at a competitive price by maintaining a good balance between time, cost, scope and quality. Furthermore, they network with professional suppliers to achieve a high level of planning, price negotiation and quality. The team at Progetto specialises in managing processes – from start to finish. The tasks include handling concepts of automation requirements through research that involves integration of solutions as part
of the production lines and process. They have successfully supplied equipment and installed projects throughout South Africa and proudly crossed borders to Angola, Kenya, Nigeria, Canada, and USA.
Q. HOW DO YOU STAY AHEAD OF INDUSTRY TRENDS AS WELL AS FOSTER INNOVATION?
We stay ahead of our business competition in the market by constantly being on the lookout for innovative and practical ways to fill the gaps in the current market with new products and services. This requires a substantial amount of investment in product development.
Q. HOW DOES THE COMPANY INTEGRATE ENVIRONMENTAL AND SOCIAL CONSIDERATIONS INTO ITS OPERATIONS?
To reduce waste, there is a recycle system in place for all our waste materials, this builds employee awareness and engagement to be more environmentally friendly. With their continuous training, creativity to design and maintaining systems we also improve their quality of life.
We as a highly motivated and skilled team committed to our customers success and requirements by exceeding their expectations, providing high quality, services, and cost with continuous improvement.
Is to lead as a preferred manufacturer and supplier in the packaging and automation industry. To provide clients with appropriate and cost-effective packaging solutions.
The team at Progetto specialises in project design and manufacturing to implementation – from start to finish. The tasks include handling concepts of automation requirements through research that involved to integrate the solutions as part of production lines and processes. They have successfully supplied equipment and install projects through South Africa and proudly crossed borders to Angola ,Kenia, Nigeria, Canada and USA.
Q. PLEASE SHARE ANY NEW PRODUCTS OR SERVICES IN THE PIPELINE?
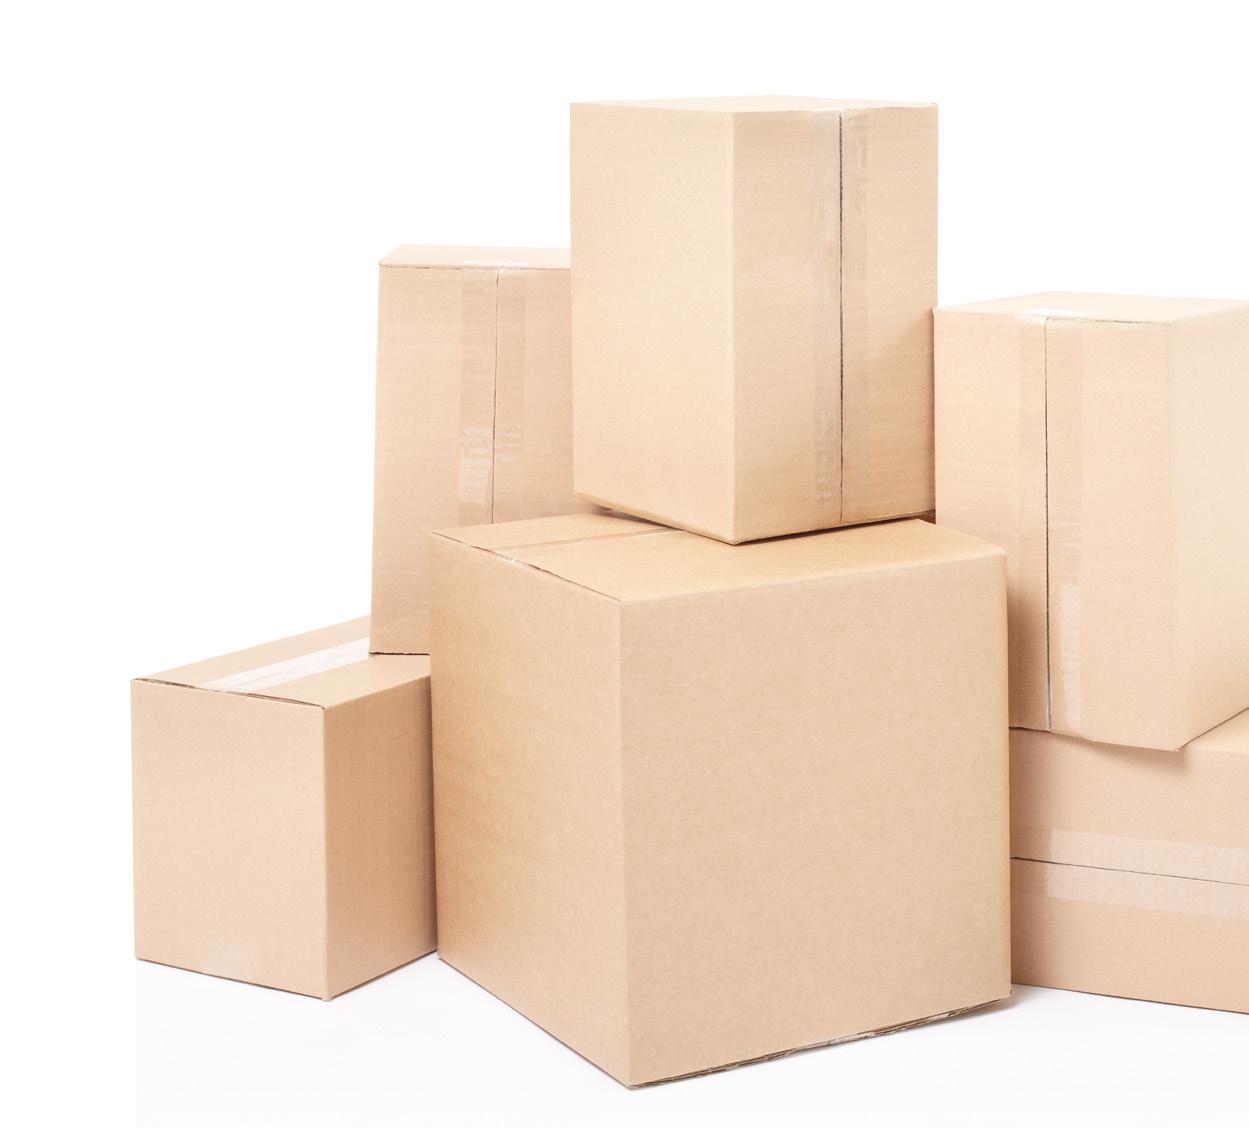
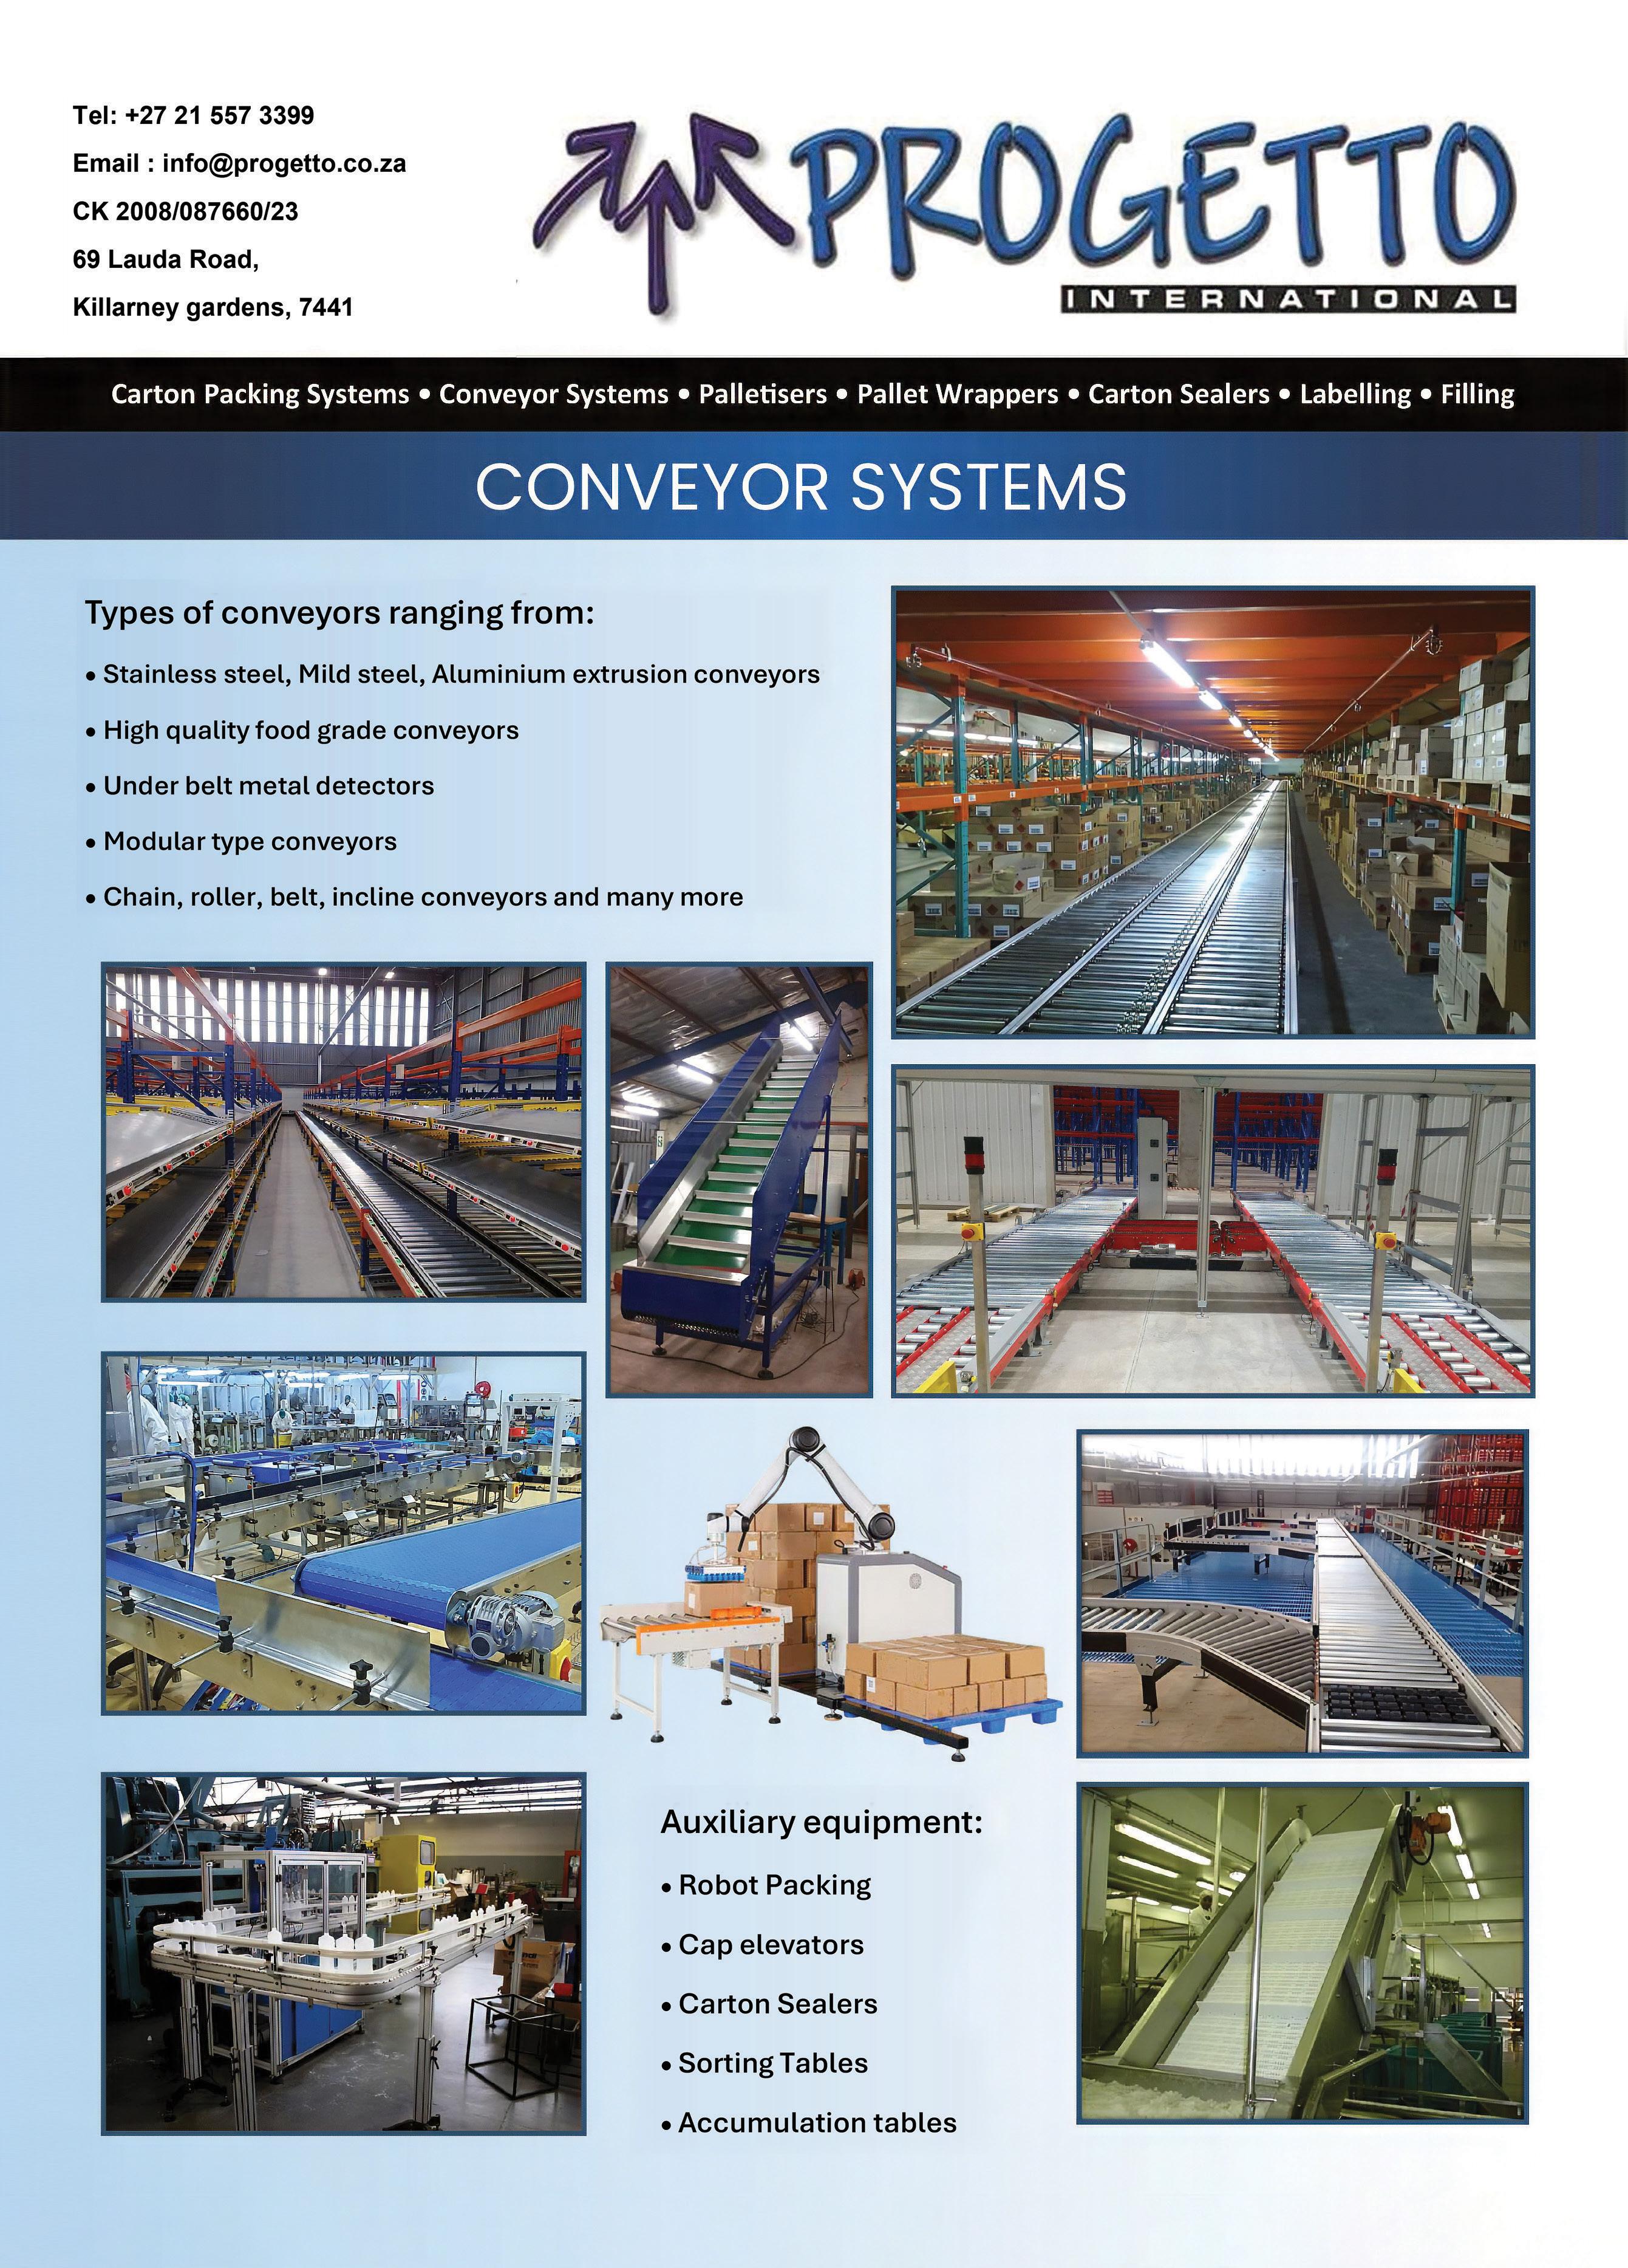
We offer a wide range of high-quality packaging systems that include the following:
• Semi-auto carton erectors for different carton sizes
• Manual and semi-automatic carton sealer for top and bottom sealing – tape or hot melt sealing
• Flow wrapping systems
• Custom built carton packing systems
• Auto filling machines for all industries e.g., cosmetic and pharmaceutical industries
• Auto and semi auto tube fillers, sealers, and trimming systems
• Pallet and shrink wrap systems.
The compact Little Gem Aspire from Urschel delivers versatile slicing, strip cutting and dicing for small- to medium-sized fresh produce processors.
The new Little Gem Aspire™ from Urschel is a compact dicer designed to deliver versatile slicing, strip cutting and dicing for processors of fruit and vegetables. Developed for small- to medium-sized processing operations, the Little Gem Aspire combines multiple cutting capabilities within a compact footprint. Designed to support operational flexibility across a wide range of fresh produce applications, the machine delivers precise cuts while supporting efficient operation, ease of use and a low total cost of ownership. Suitable for a variety of fruit and vegetable applications, the Little Gem Aspire can process products including onions, potatoes, apples, carrots, tomatoes, beetroot and mango. The machine can produce slices from 2 mm to 20 mm, along with a range of strip cuts and dices up to 20 mm.
Heat and Control has been the exclusive Urschel representative in Africa since 1950 — with more than 30 offices worldwide.
“Multiple cuts. One compact machine. Low cost of ownership.”
“One of the key advantages of Little Gem Aspire is its versatility across multiple fruit and vegetable applications,” says Jeff Rossouw, Heat and Control General Manager South Africa. “Fresh produce naturally varies in size, density and moisture content, so processors
Established in 1950, Heat and Control is a privately owned company with a global team that has built an extensive knowledge bank and developed a wealth of experience and expertise. Access to production and technical support from a network of engineers, food technicians, field service technicians, skilled tradespeople and support teams provides food manufacturers with the confidence to achieve their production goals.
require equipment capable of delivering consistent, precise cuts across different products and applications. The Little Gem Aspire combines multiple cutting capabilities within a single machine, allowing processors to quickly transition between products while achieving
Urschel designs and manufactures high capacity, precision food cutting machinery designed for rugged production environments.
Sanitary and dependable in design. Rely on Urschel cutting solutions to effectively process all types of products.
Explore more cutting solutions at heatandcontrol.com/urschel
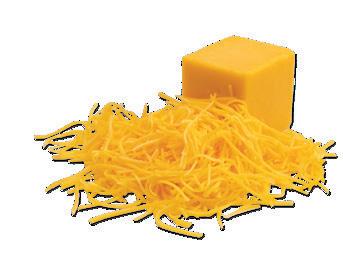
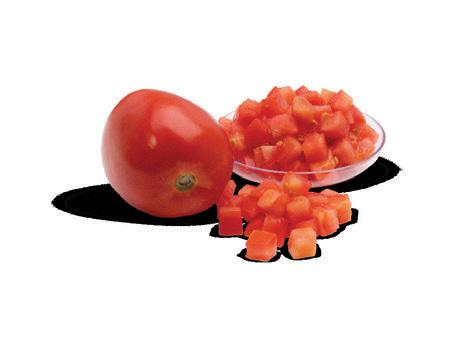
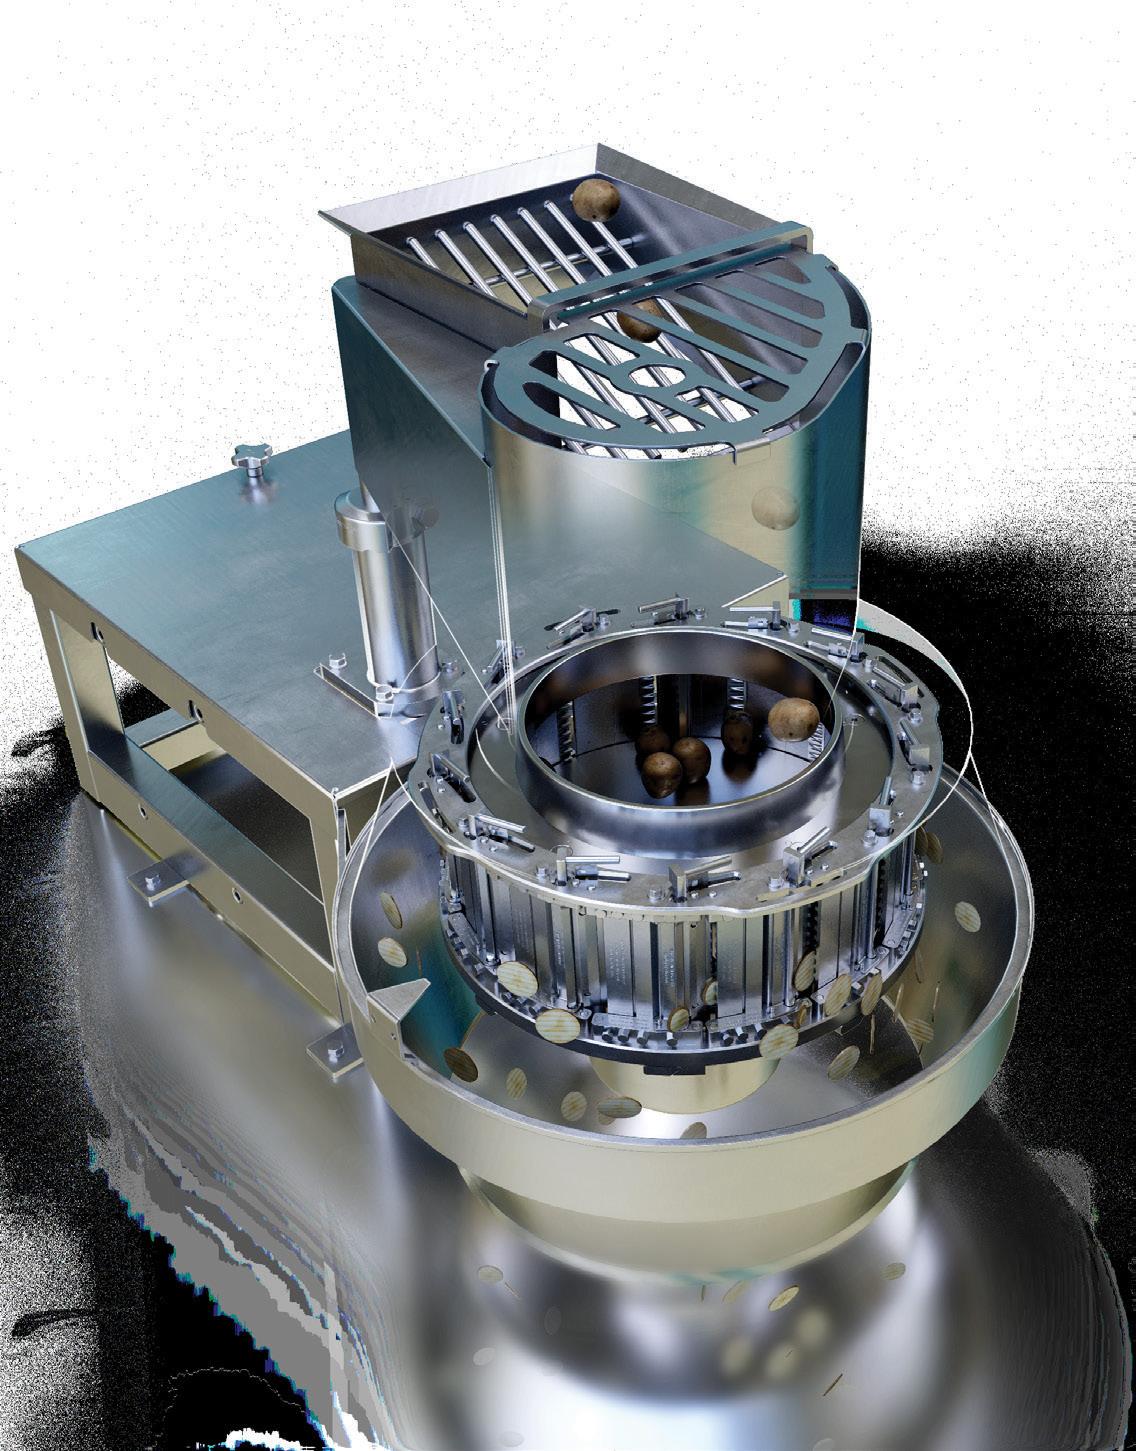
Designed for small- to medium-sized processors, the new Little Gem Aspire supports flexible fruit and vegetable cutting applications.
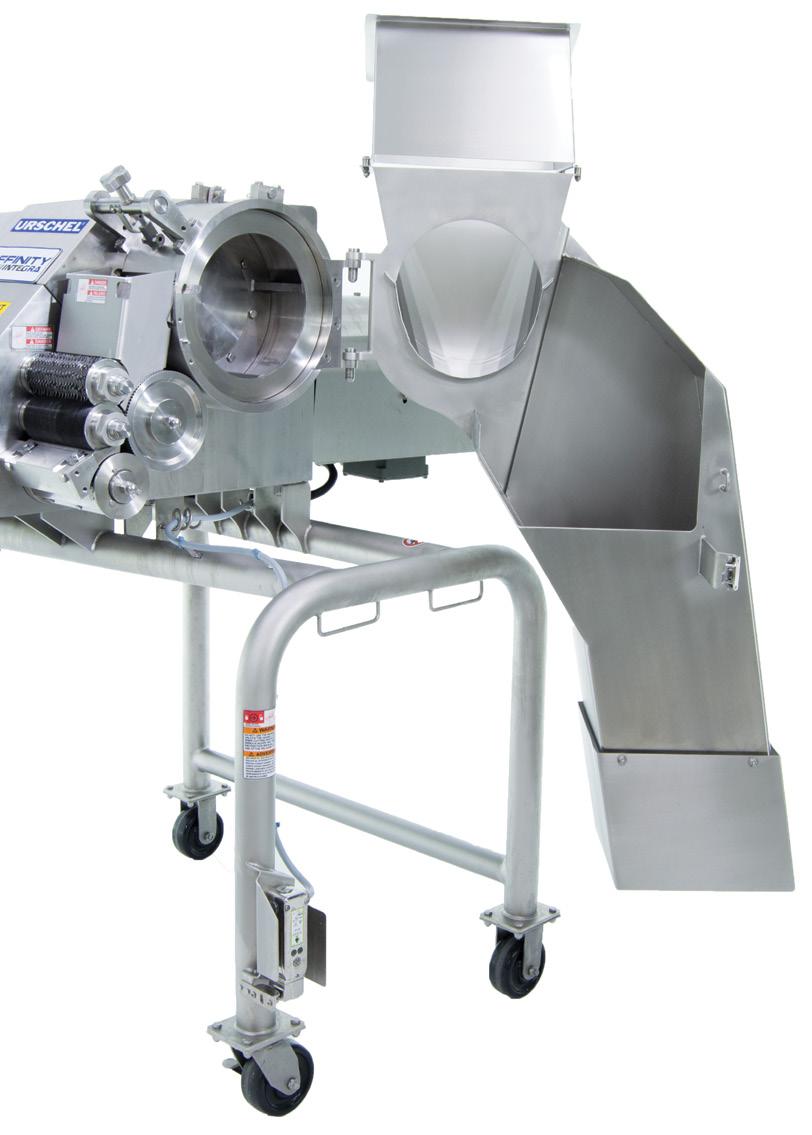
Compact footprint, low total cost of ownership: As processors continue looking for ways to maximise production flexibility without increasing line footprint, compact equipment capable of handling multiple cutting applications within a single machine is becoming increasingly valuable. Engineered for a low total cost of ownership — from initial investment through to ongoing operation — the Little Gem Aspire is designed to support efficient processing while simplifying operation and maintenance requirements.
Key features of the Little Gem Aspire include a compact footprint to support efficient line integration, multiple cut styles from a single machine and a wide cutting range. The machine features Urschel’s StatiCut™ knife assembly technology, designed to simplify changeovers between cut sizes while reducing the number of parts requiring maintenance and inventory.
“These features make the Little Gem Aspire an ideal solution for fruit and vegetable processors seeking efficiency, versatility and low cost of ownership,” says Rossouw. Heat and Control is the exclusive representative of Urschel equipment in Africa, offering cutting sets, spare parts and product testing services.
Twelve manufacturing, warehouse and associated facilities, 10 test centres, more than 30 offices globally. Testing, design, engineering, manufacturing, installation, commissioning, user training, spare parts and after-sales service.
Cutting range: Slices from 2 mm to 20 mm; strip cuts and dices up to 20 mm
Products processed: Onions, potatoes, apples, carrots, tomatoes, beetroot, mango and more
Footprint: Compact design for efficient line integration
Cut styles: Slicing, strip cutting and dicing from a single machine
Knife technology: Urschel StatiCut’ knife assembly for fast, simple changeovers
Cost of ownership: Engineered for low total cost from initial investment to ongoing operation
Support: Cutting sets, spare parts and product testing services available through Heat and Control
Heat and Control: Exclusive Urschel representative in Africa — 12 facilities, 10 test centres, 30+ offices
Seal Global, in partnership with BASF, is challenging South Africa's FMCG and QSR sectors to move beyond recycling rhetoric — offering proven, science-backed barrier coatings that make sustainable food packaging an operational reality today.
As South Africa’s FMCG and quick-service restaurant (QSR) sectors face mounting pressure to reduce plastic waste, the conversation is shifting away from theoretical recycling models toward immediate, practical end-of-life realities. The true challenge? Eliminating plastics without compromising food safety, shelf life, or operational margins.
For years, the food packaging industry has relied on a compromise. To achieve the rigorous barrier properties required for grease resistance, moisture retention, and oil barriers, paper packaging has traditionally been laminated with thin layers of polyethylene (PE) or aluminium foil. While these composite materials successfully protect the food, they create a secondary crisis at their end-of-life: they do not break down naturally, and they cannot be processed by standard South African paper mills. They are destined to remain in landfills or the environment indefinitely.
"True sustainability isn't about idealistic concepts; it's about what actually happens to a package when it is discarded," says the team at Seal Global, a South African leader in sustainable packaging innovations. "If a package cannot easily wash out in a standard paper mill or degrade naturally in the environment, it isn't a solution. True environmental responsibility requires a fundamental shift in packaging chemistry."
WATER-BASED BARRIER TECHNOLOGY
To solve this friction point between performance and environmental impact, Seal Global has pioneered a range of proprietary, water-based dispersion coatings. By partnering globally with chemical giant BASF, Seal Global applies advanced polymer science directly to renewable, paper-based substrates.
"True sustainability isn't about idealistic concepts; it's about what actually happens to a package when it is discarded."
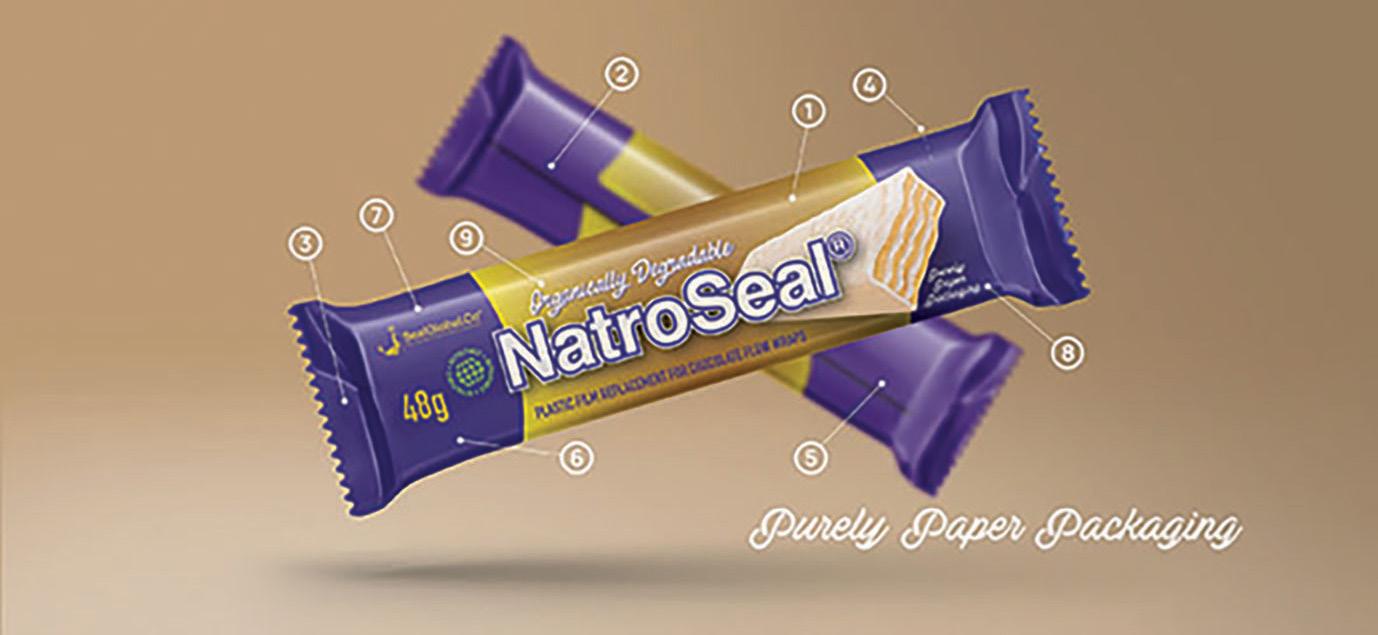
The result is Paperised Packaging™ a portfolio of coatings that replace traditional plastic linings with a microscopic, high-performance barrier. Once discarded, these coated papers are completely water-soluble during standard repulping processes and degrade in the environment.
For food manufacturers and QSR brands looking to make a measurable impact in this month’s Food Sustainability focus, three core innovations are leading the charge:
• FastSeal® (The QSR solution): Traditional fast-food packaging for greasy foods typ-
Developed in partnership with BASF, Seal Global's water-based dispersion coatings replace traditional plastic and foil laminates — and are engineered to run on standard printing and converting equipment, requiring no specialist machinery.
• FastSeal® — Grease, oil and condensation resistance for QSR packaging; 100% repulpable and plastic-free
• CupSeal® — Replaces internal plastic cup linings; enables single-use cups to be repulped or biodegrade if littered
• SilvaSeal® & GoldSeal® — Foil and LDPE replacements for butter and spread wraps; converts to metallic monoweb paper that is fully degradable and repulpable
All products are water-soluble during standard repulping and degrade naturally in the environment — supporting South Africa's growing Extended Producer Responsibility (EPR) compliance obligations.
ically relies on PE-laminated board. FastSeal® provides exceptional grease, oil, and condensation resistance without a plastic film. Because it is completely plastic-free, the paper is 100% repulpable in standard mill processing while simultaneously offering a 15% material yield savings for commercial kitchens.
• CupSeal® (Rethinking the single-use cup): By replacing the internal plastic lining of hot and cold beverage cups with a low-temperature, water-dispersion coating, CupSeal® ensures that single-use cups can be easily repulped alongside standard cardboard and paper waste or break down naturally if they leave the waste stream.
• SilvaSeal® & GoldSeal® (Degradable dairy & spread packaging): Historically, butter and margarine wraps required a complex multi-layer laminate of foil and low-density polyethylene (LDPE). SilvaSeal® enables a single-process conversion onto a brilliant metallic monoweb paper that preserves freshness but is fully degradable and repulpable.
What makes this chemical evolution particularly vital for the local market is its seamless integration into existing infrastructure. Packaging converters do not need to invest in specialised, high-cost machinery to adopt Seal Global’s technology; these coatings are engineered to run efficiently on standard printing and converting equipment.
CCL Industries announces closing of Sleever international acquisition, strengthening global sleeve and film capabilities.
CCL Label (“the Company”), a world leader in specialty label, security and packaging solutions, today announced the closing of its acquisition of Sleever International Company SA, its subsidiaries, and related companies (“Sleever”). Sleever is a privately owned global manufacturer of shrink sleeve labels, extruded films, and application equipment serving consumer packaged goods and healthcare customers.
Following the closing, Sleever’s label and film businesses will be rebranded as CCL Label and Innovia Films, respectively. Sleever’s application equipment business will continue to operate under the Sleever name, preserving its strong reputation in machinery and engineering.
The acquisition significantly expands CCL’s global footprint and technical capabilities in the growing sleeve and film segments. Customers across consumer-packaged goods, food & beverage, beauty, home care, and healthcare markets will benefit from:
• Broader global supply coverage, with Sleever’s 11 manufacturing sites joining CCL’s worldwide network to improve supply chain resilience, shorten lead times, and enhance business continuity.
• A more comprehensive portfolio of sustainable materials, including recycling-friendly and low-impact sleeve solutions, advanced films, and energy-efficient application systems that support customers’ environmental commitments.
• Stronger innovation capabilities, combining CCL’s and Sleever’s R&D strengths to accelerate development of next-generation sleeve formats, improved recyclability technologies, and high-performance films.
• Integrated decoration and application expertise, enabling customers to achieve premium shelf impact, reduce waste, and improve operational efficiency through ad-
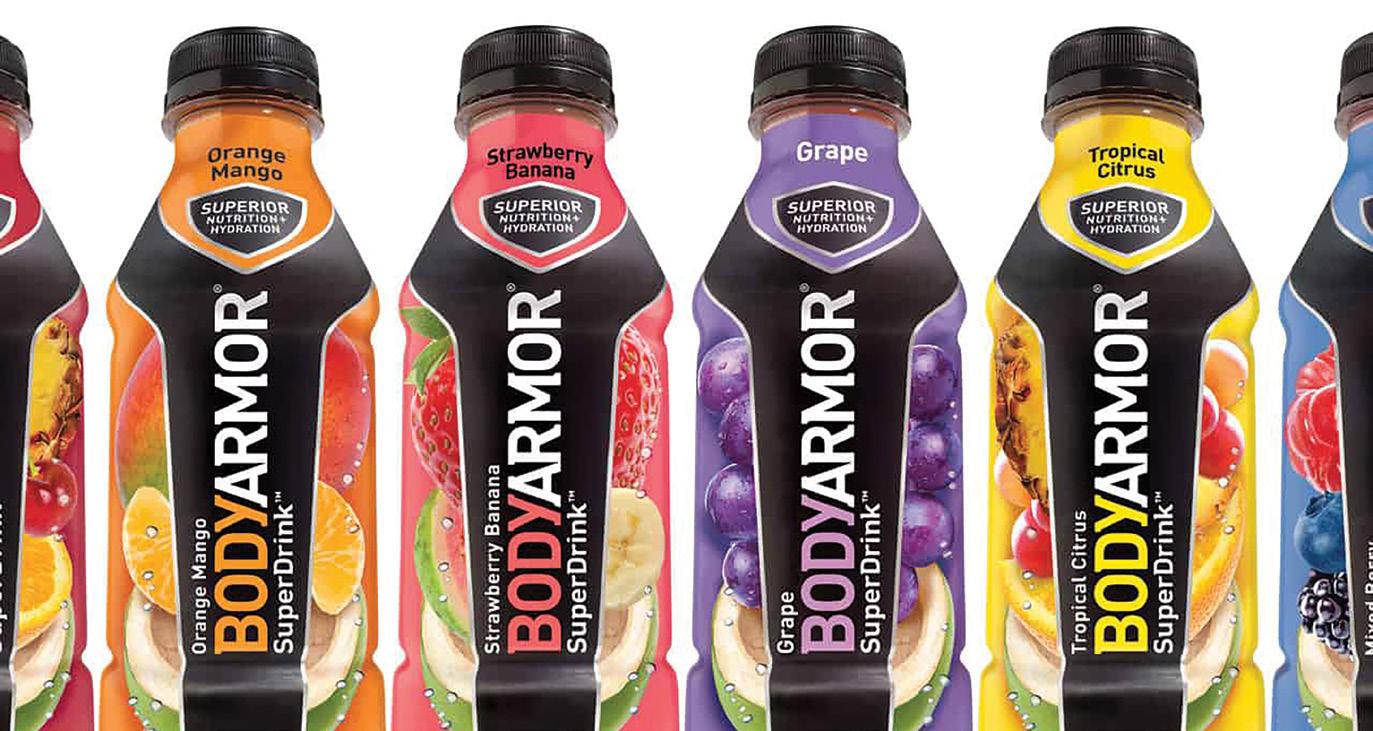
vanced application equipment and high-end decoration services.
• Greater technical support and engineering depth, with expanded global teams providing end-to-end expertise from material science to application equipment.
CCL Industries' integration of Sleever International delivers a range of immediate and long-term benefits across the supply chain:
• Greater supply resilience — Broader global footprint means shorter lead times and stronger business continuity
• Expanded sustainable materials — A wider portfolio of recycling-friendly and low-impact sleeve and film solutions
• Energy-efficient application systems — Advanced machinery designed to support customers' environmental commitments
• Combined R&D power — Joint technical teams accelerating next-gen sleeve formats and recyclability technologies
• End-to-end expertise — Integrated decoration, application, and material science support from a single partner.
"Bringing Sleever into the CCL family significantly strengthens our ability to serve customers in the sleeve and film markets."
Günther Birkner, president of CCL Label’s food & beverage sector and Innovia Films, who will assume overall responsibility for the acquisition, commented: “Bringing Sleever into the CCL family significantly strengthens our ability to serve customers in the sleeve and film markets. By combining Sleever’s deep expertise in shrink sleeve technology and application equipment with CCL’s global scale and portfolio, we are creating a more resilient, innovative, and further customer-focused platform. This acquisition allows us to offer broader sustainable solutions, enhanced technical support, and greater supply security—benefits that will help our customers compete and grow in their markets.”
CCL - www.cclind.com
Sleever International - www.sleever.com
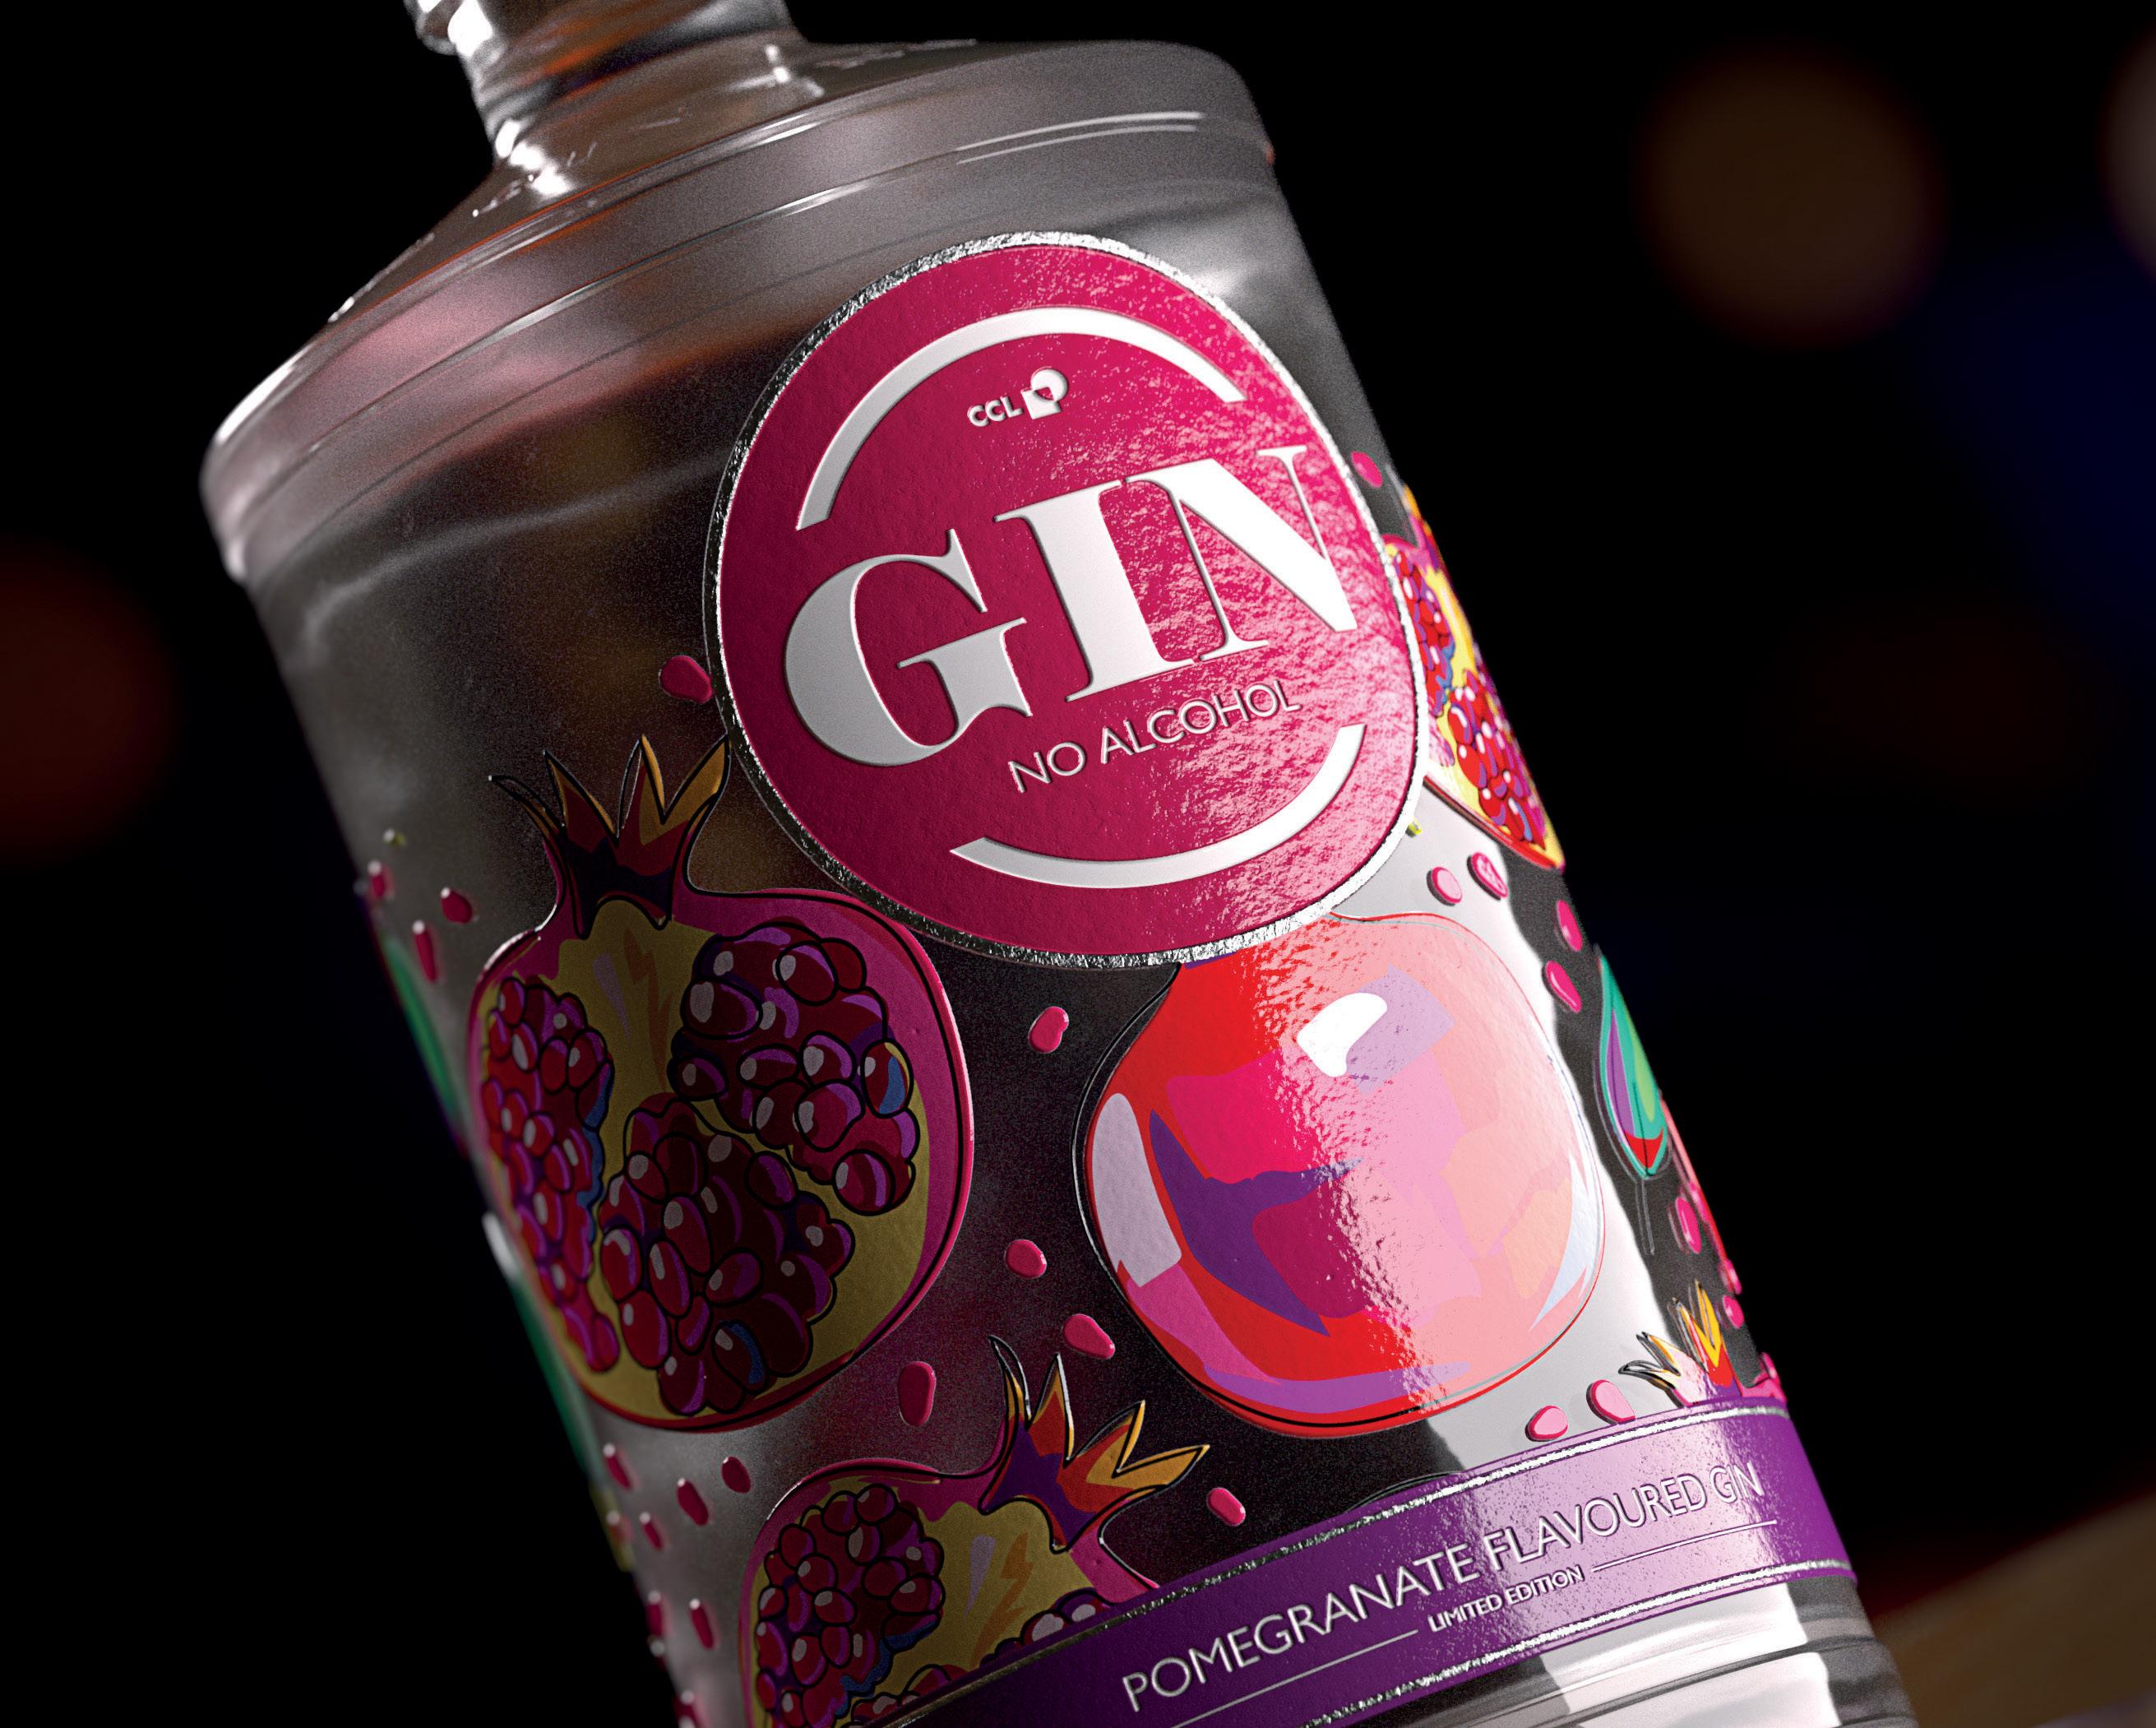
From the gym to the great outdoors, proper hydration goes beyond drinking water. Electrolytes are the unsung heroes of peak performance — and with the right mineral salt formulations, brands can deliver products that truly make a difference.
tion, keeping people energised and performing well at work throughout the day. Travel: Long flights, busy schedules, and changing environments can quickly lead to dehydration. Electrolyte products help maintain hydration, so travelers feel refreshed and alert.
Whether someone is working, exercising, traveling, or simply relaxing, staying hydrated is essential for maintaining energy and supporting performance. Our high-quality mineral salts provide a strong foundation for electrolyte products that help with hydration in all these situations.
Exercise: Athletes rely on electrolytes to stay hydrated and avoid muscle cramps. Electrolyte formulations are well suited for pre workout, post workout, and performance focused products.
Physical labour: People in physically demanding jobs, such as construction or warehousing, lose significant fluids and Minerals through sweat. Electrolyte solutions help replace these Minerals and support hydra-
Hot weather: High temperatures and outdoor activity increase sweat loss. Electrolyte solutions help maintain fluid balance, reduce the risk of cramps, and support recovery in hot conditions.
Electrolytes such as Magnesium, Calcium, and Potassium are essential for fluid balance, muscle function, and overall performance. Using our high value Mineral Salts helps hydration products deliver ultimate functionality and a great taste. The clever combination of Minerals ensures that electrolyte solutions are effective and enjoyable and deliver superior performance.
Magnesium, calcium, and potassium work together to support fluid balance, muscle function, and overall performance — making them the cornerstone trio of any effective electrolyte formula.
"The clever combination of mineral salts ensures that electrolyte solutions are effective and enjoyable — and deliver superior performance."
Magnesium Hydrogencitrate and Magnesium Citrate Malate: Valuable sources of Magnesium that supports muscle function and helps prevent cramps. Ideal for hydration products focused on muscle recovery and reducing fatigue.
Calcium Lactate PLUS: Highly soluble and mild in flavor. Supports muscle contraction and nerve function while contributing to effective hydration.
Potassium Magnesium Citrate: Important for fluid balance, nerve and muscle actions, with a clean taste and no bitterness that works well in hydration drinks.
Along with supplying high quality mineral salts, we offer prototype recipes and expert support to help you develop effective electrolyte products. Whether you are working on sports drinks, supplements, or functional hydration beverages, we are here to assist throughout the development process.
Our Mineral Salts – including Magnesium Hydrogencitrate, Magnesium Citrate Malate, Potassium Magnesium Citrate and Calcium Lactate PLUS – are ideal for creating hydration solutions that consumers trust. From fitness hydration to recovery and travel ready products, we help you develop electrolyte formulations that stand out in the market.
Explore our Mineral Salts and start creating high-performance electrolyte formulations. Contact local sales partner Nautilus Chemicals to request more information or samples.
Nautilus Chemicalswww.nautiluschemicals.co.za Dr. Paul Lohmann GmbH & Co. KGaAwww.lohmann-minerals.com
Founded in April 2019 by the Warren brothers, Nautilus Chemicals (Pty) Ltd. brings together over 35 years of combined experience in the mineral and chemical supply industry. With backgrounds spanning both science and commerce, and a shared passion for the products and the sector, the brothers have built a company grounded in expertise, integrity, and dedication to excellence.
The company specialises in the sourcing and supply of premium raw materials to the food and beverage, pharmaceutical and health supplement, and veterinary industries across Southern Africa. Our portfolio is carefully curated, ensuring that only the finest materials reach our clients — materials which form the foundations of quality end-products.
We import exclusively from highly regarded manufacturers, bringing world-class standards to the South African market. Our warehousing facilities enable efficient distribution throughout South Africa and into the broader sub-Saharan region, ensuring reliability and consistency at every stage.
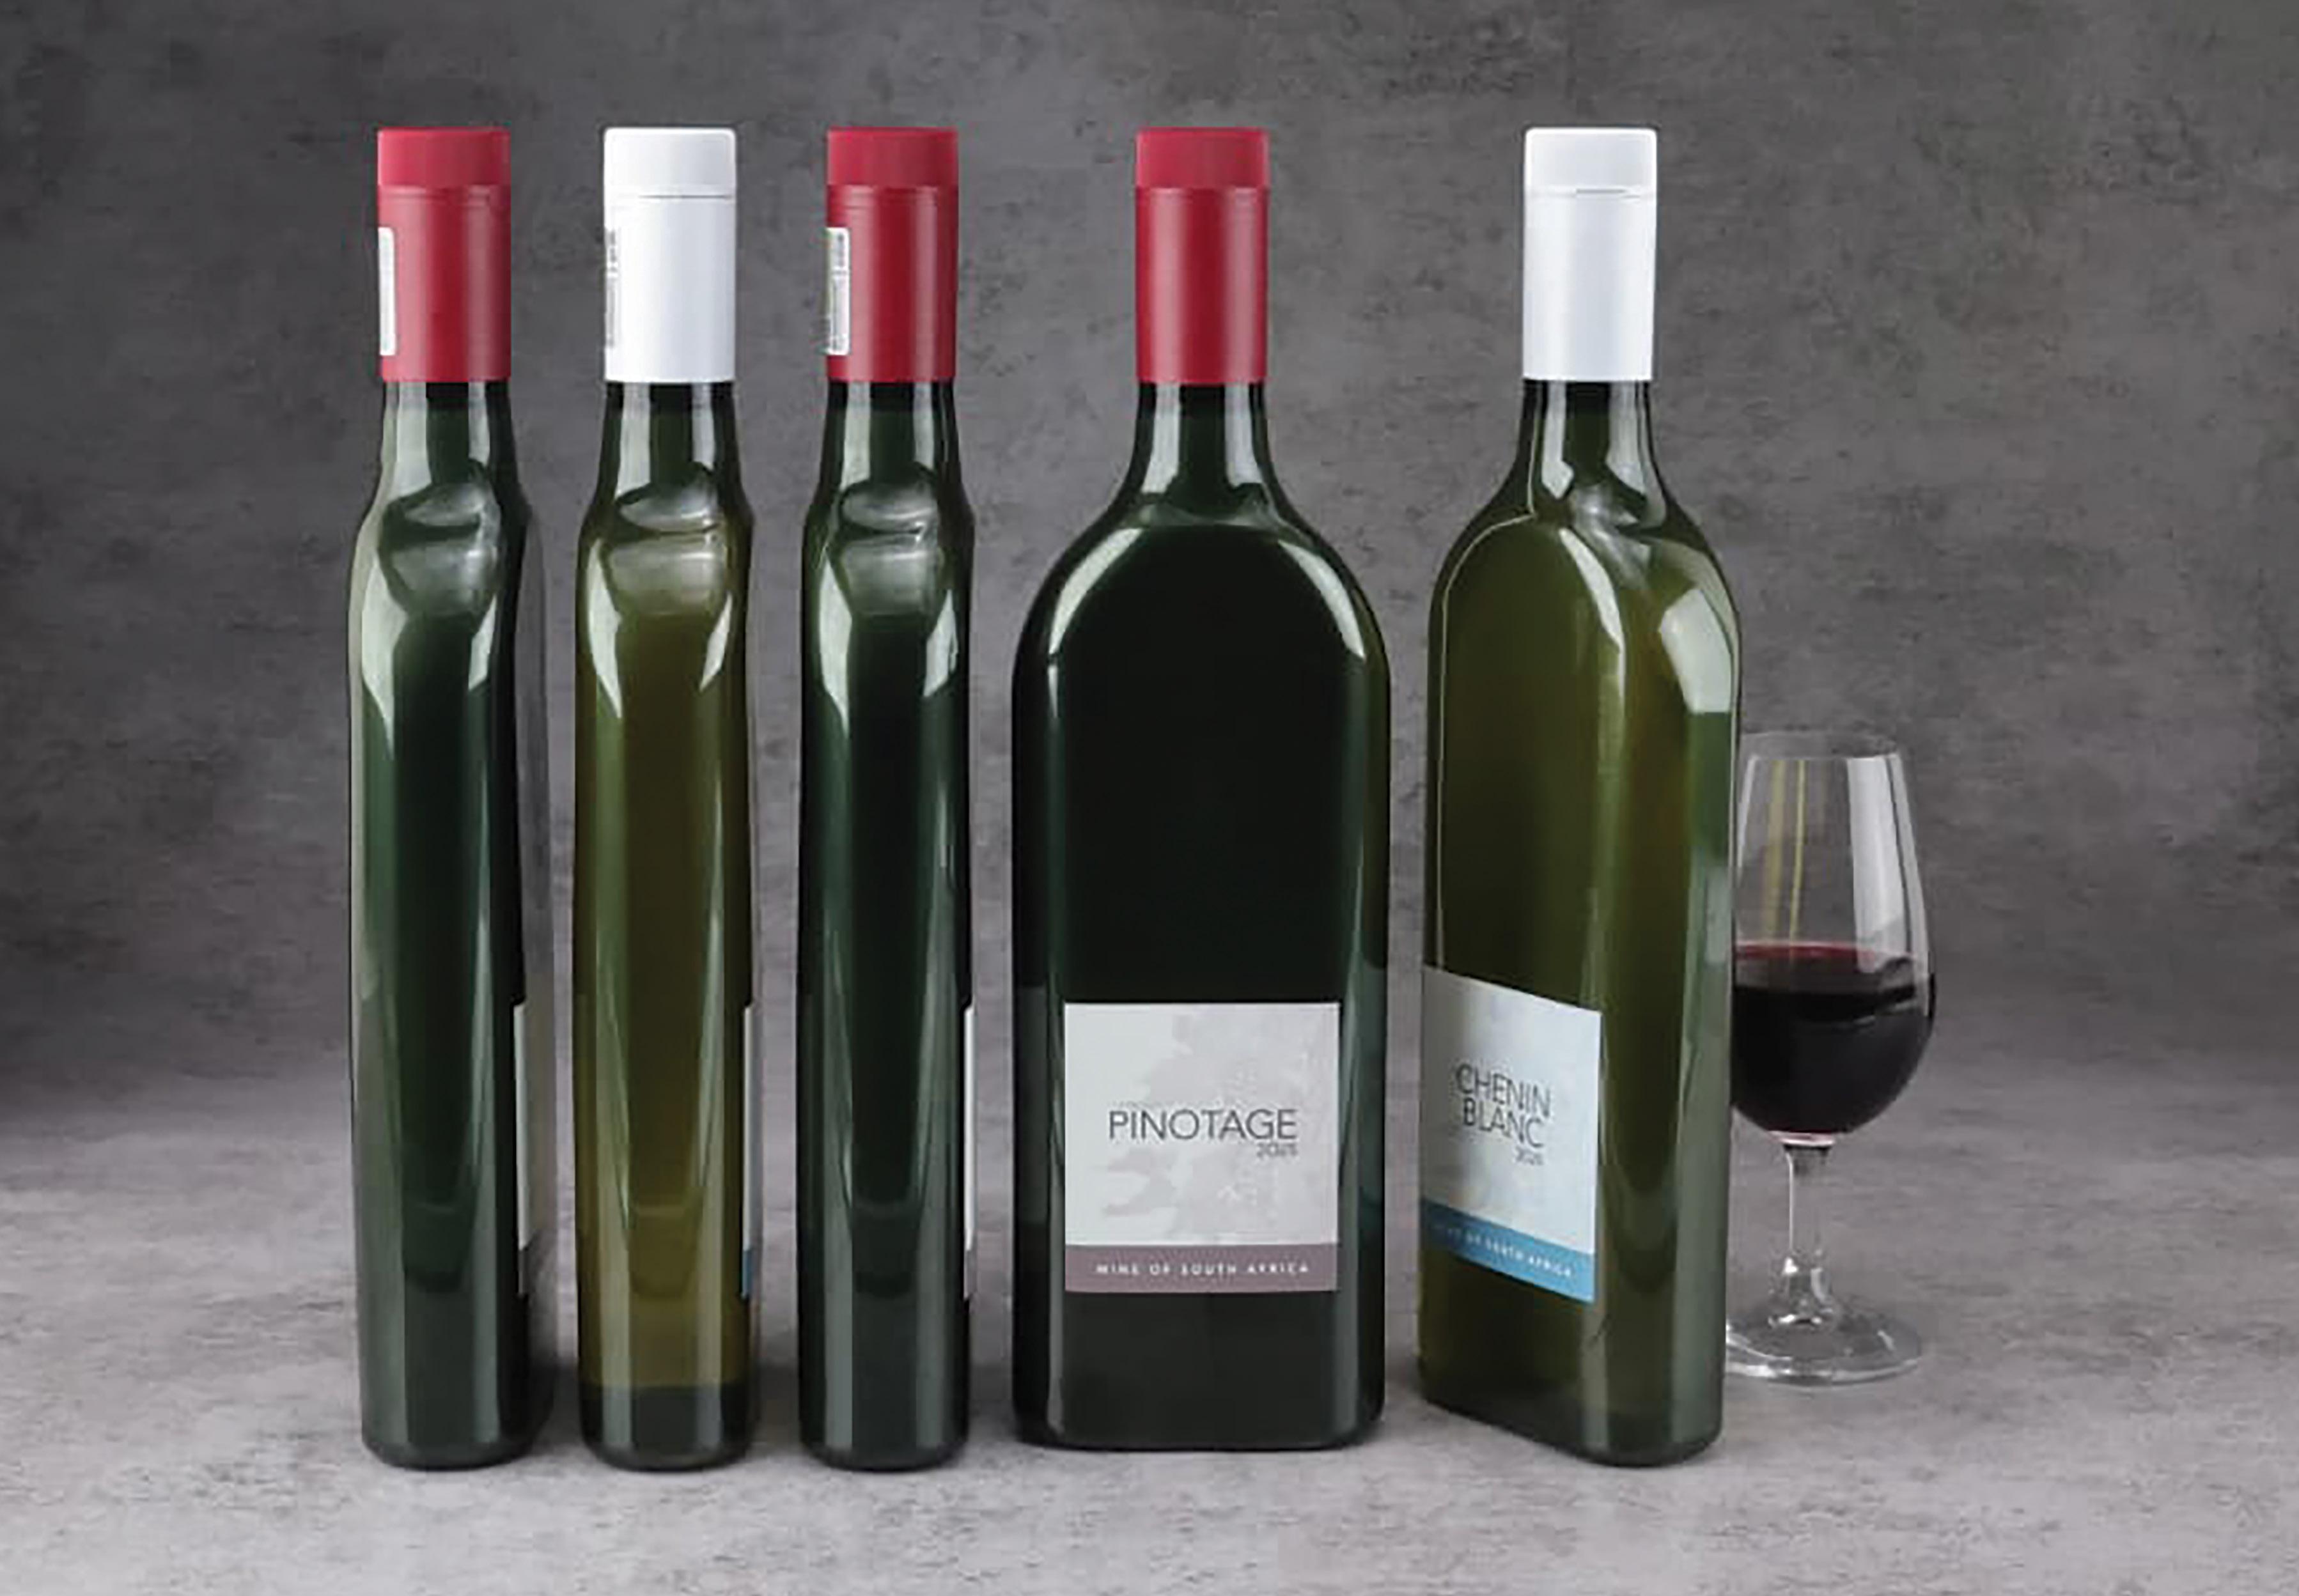
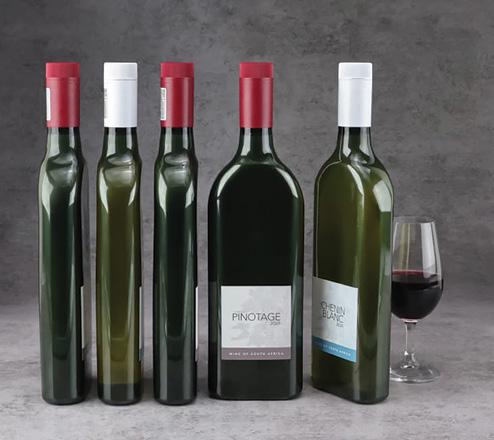
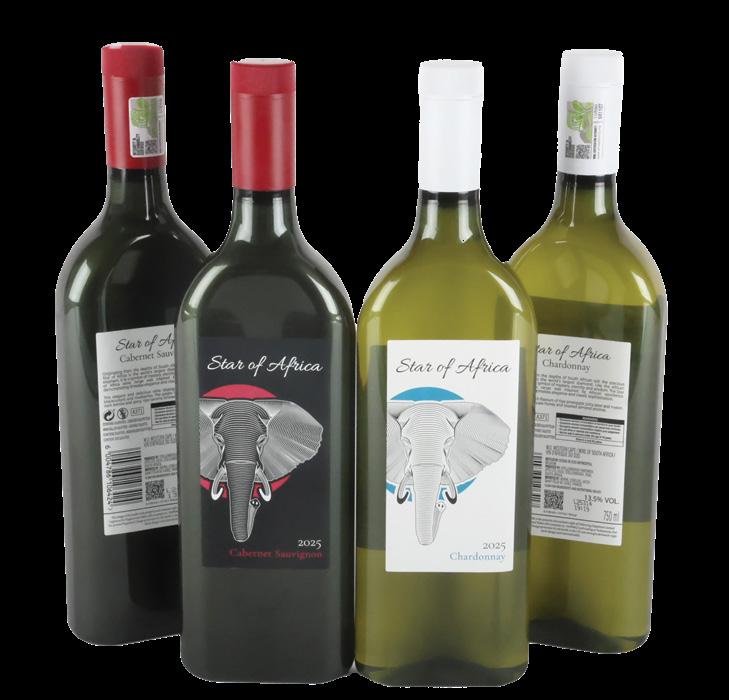
Polyoak Packaging, in collaboration with Packamama, Safripol and Stellenbosch Vineyards, has launched South Africa’s first eco-flat wine bottle.
Polyoak Packaging, in partnership with Packamama, Safripol and Stellenbosch Vineyards, has introduced the novel Eco-Flat Wine Bottle to the South African wine market, offering a lightweight and space-efficient packaging format designed to support sustainability targets and improve supply chain efficiency for wine producers.
Manufactured locally by Polypet, part of Polyoak Packaging, the 750 ml Eco-Flat Wine Bottle is produced using Packamama’s patented flat-bottle design and weighs just 63 g, making it up to 80% lighter than a traditional glass wine bottle. The reduced weight and distinctive flat profile enable significant efficiencies in transport and storage, helping producers to lower logistics costs while reducing associated carbon emissions.
The bottle is produced using AspireR25, a recycled PET (rPET) resin developed by Safripol. AspireR25 contains 25% locally sourced post-consumer rPET, collected and recycled in South Africa and converted into
premium-grade material for wine bottles. The bottle is converted at Polyoak’s worldclass manufacturing facility in Cape Town, ensuring consistent quality and reliable supply for the wine industry.
Life cycle assessment (LCA) data for PET bottles clearly demonstrates that replacing virgin PET with recycled PET delivers substantial environmental benefits across key impact categories, including reductions in carbon emissions, energy consumption and resource use. By incorporating post-
“The Eco-Flat Wine Bottle provides producers with a practical packaging solution that delivers both sustainability and operational advantages.”
consumer recycled content, the Eco-Flat Wine Bottle contributes to a more circular packaging solution, while supporting the broader sustainability goals of the wine sector.
Supporting South African jobs and a circular economy: Importantly, the use of locally sourced recycled material also actively sustains local jobs by creating market demand for post-consumer resin, strengthening South Africa’s recycling value chain and supporting the development of a circular plastics economy.
The Eco-Flat Wine Bottle is available in dead leaf green and colourless formats and can be paired with a range of closure colours, offering flexibility for producers across different wine styles and brand portfolios. An integrated oxygen barrier provides a shelf life of up to 24 months,
making the format well suited to all still wines produced for easy drinking.
Smarter packing, lower carbon footprint: The flat bottle format also delivers measurable supply chain efficiencies. The design allows bottles to be cross-packed and flat-packed, improving space utilisation throughout distribution. Compared with traditional glass bottles, the format is up to 40% more space-efficient per pallet, enabling greater transport density and reducing the overall carbon footprint of wine shipments. “The wine sector is under increasing pressure to reduce its environmental impact while
Polyoak Packaging is one of the leading rigid plastic packaging suppliers in Southern Africa. It comprises numerous
maintaining product quality and brand integrity. By combining recycled materials with a more efficient bottle design, the EcoFlat Wine Bottle provides producers with a practical packaging solution that delivers both sustainability and operational advantages,” Roger Kerr, sales executive, Polyoak Packaging.
The innovation has already received industry recognition, with Polyoak Packaging being nominated in the Western Cape Economy Innovation Awards, hosted by the Cape Chamber of Commerce and Industry. This acknowledgement highlights the role of the Eco-Flat Wine Bottle in advancing sustainable packaging innovation while boosting the
competitiveness of South African wine producers. With global markets increasingly focused on carbon reduction and responsible packaging, the Eco-Flat Wine Bottle provides the South African wine industry with a scalable, locally produced packaging alternative that aligns with evolving trade requirements while strengthening the country’s circular economy.
63 g bottle weight - up to 80% lighter than glass
750 ml standard format, suitable for all still wines
25% post-consumer rPET content
(AspireR25 by Safripol)
24 months shelf life provided by integrated oxygen barrier
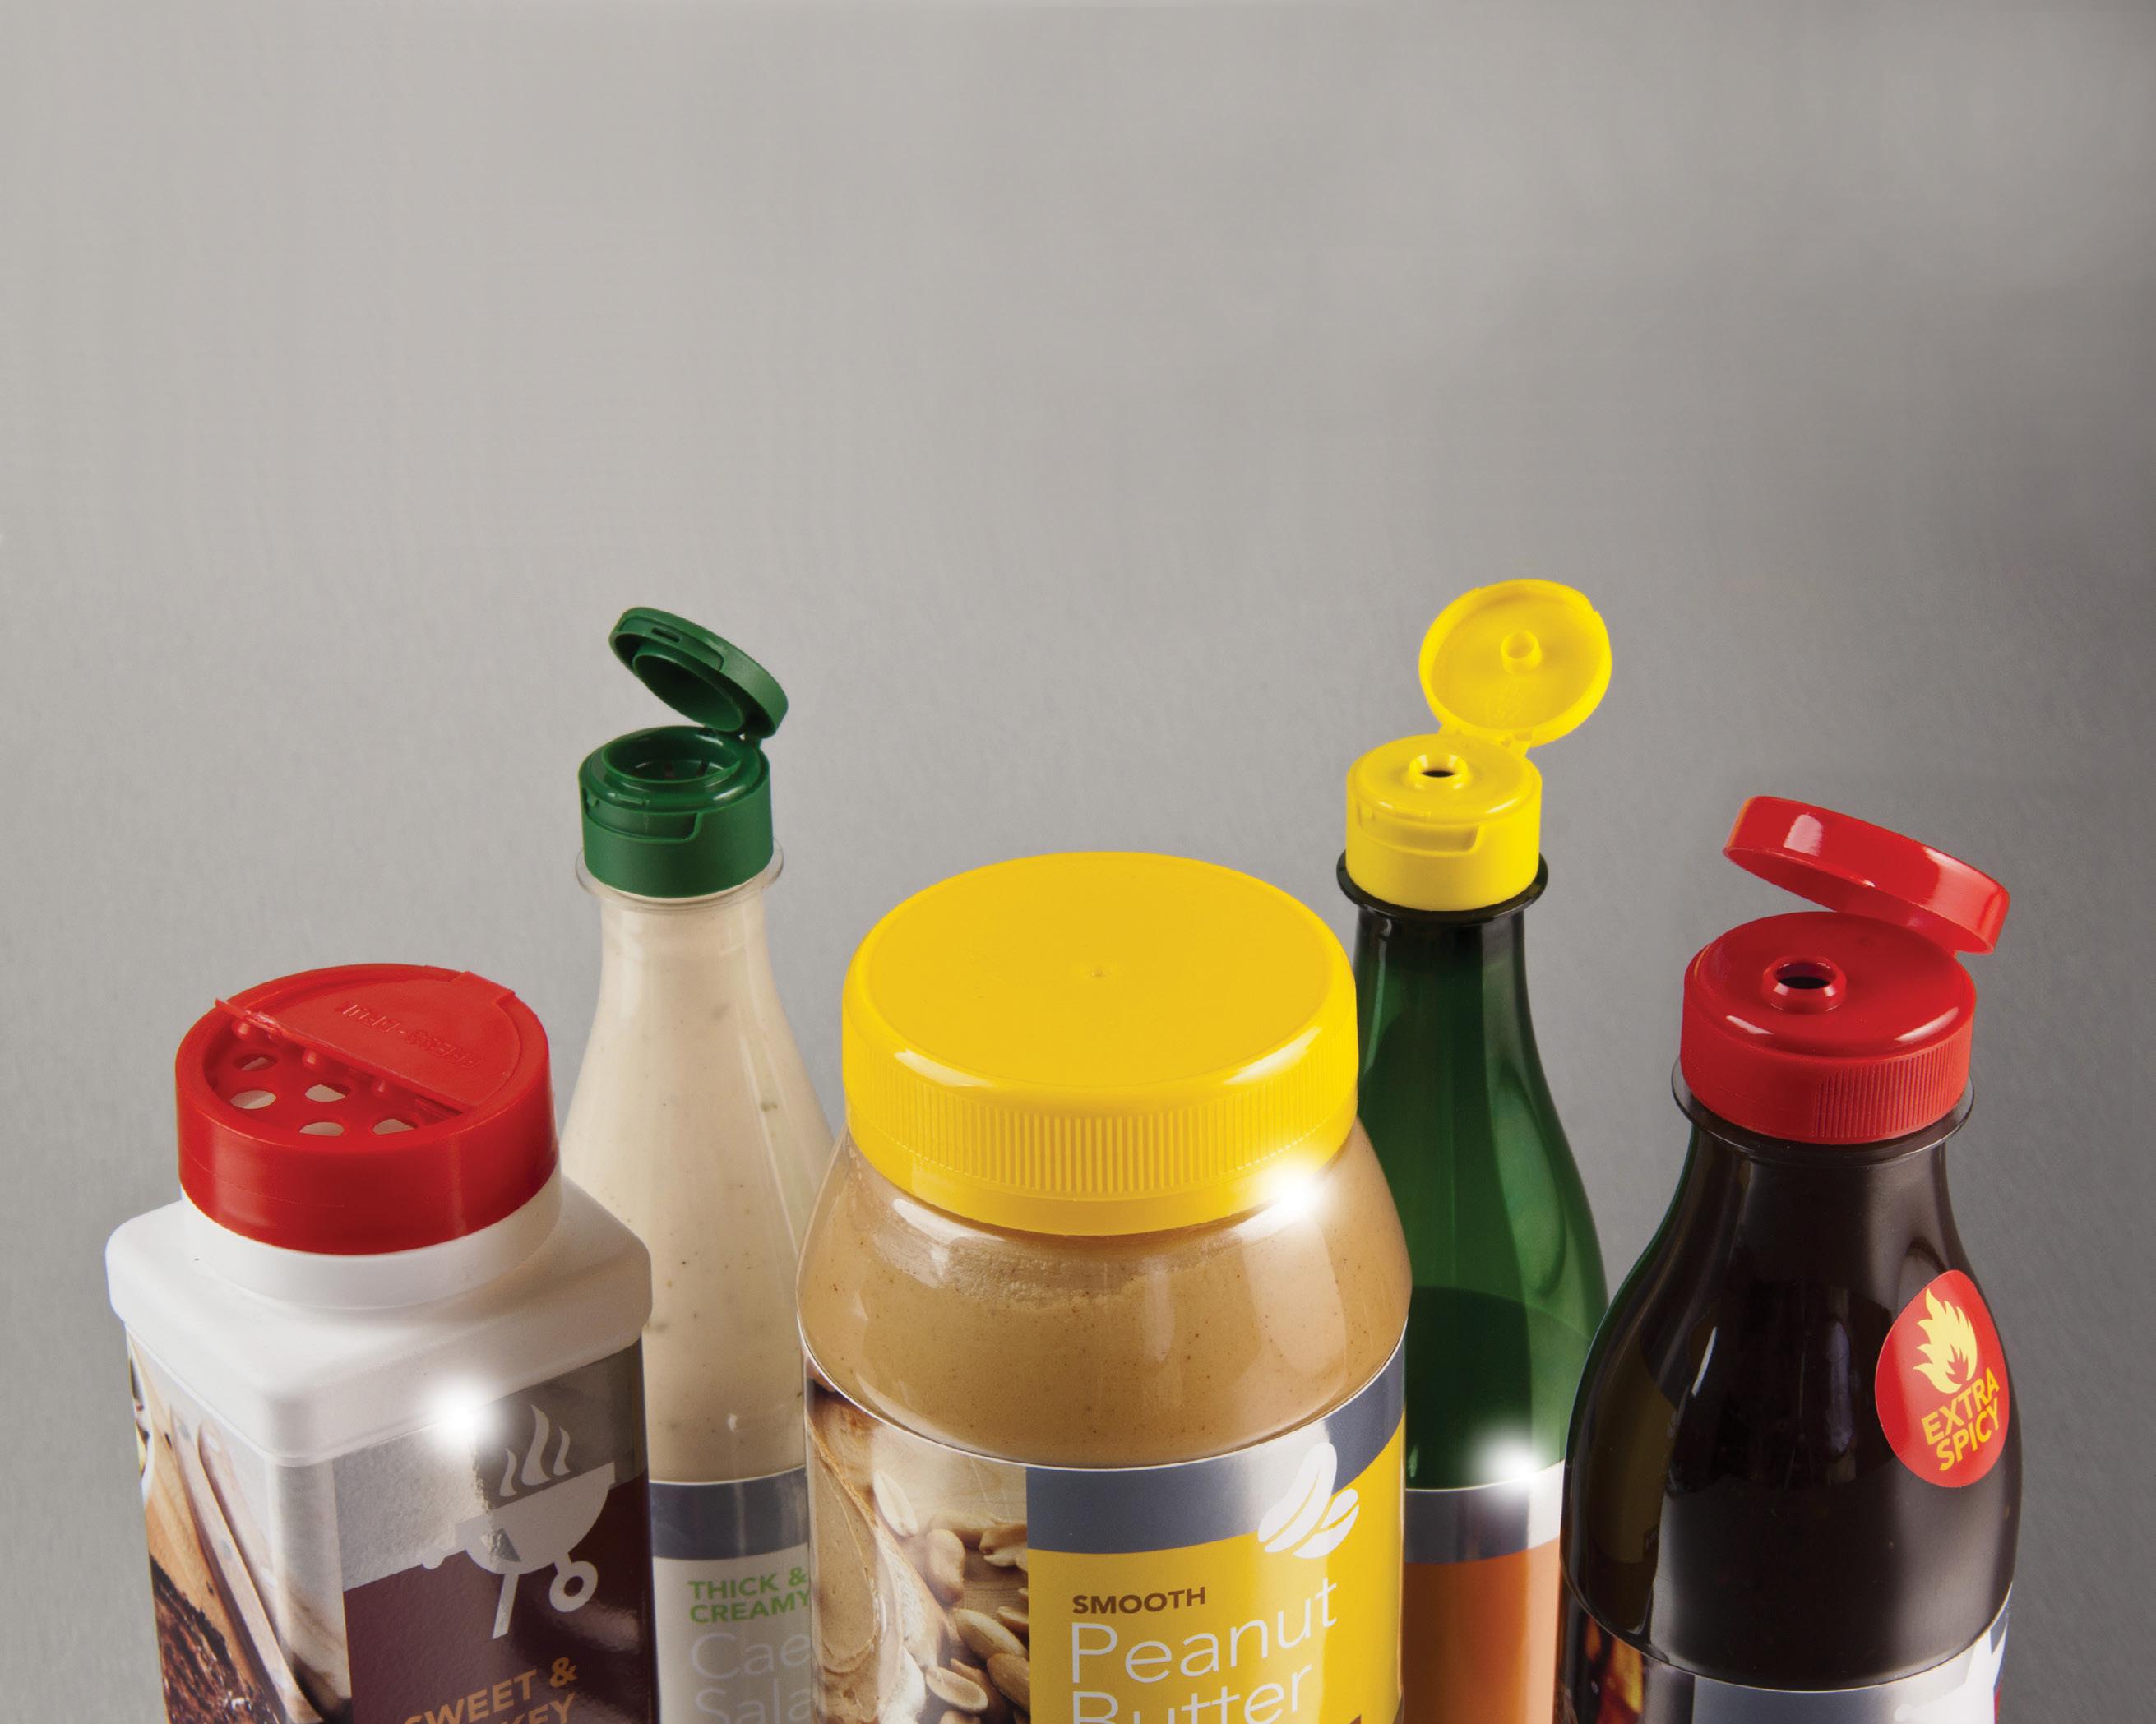
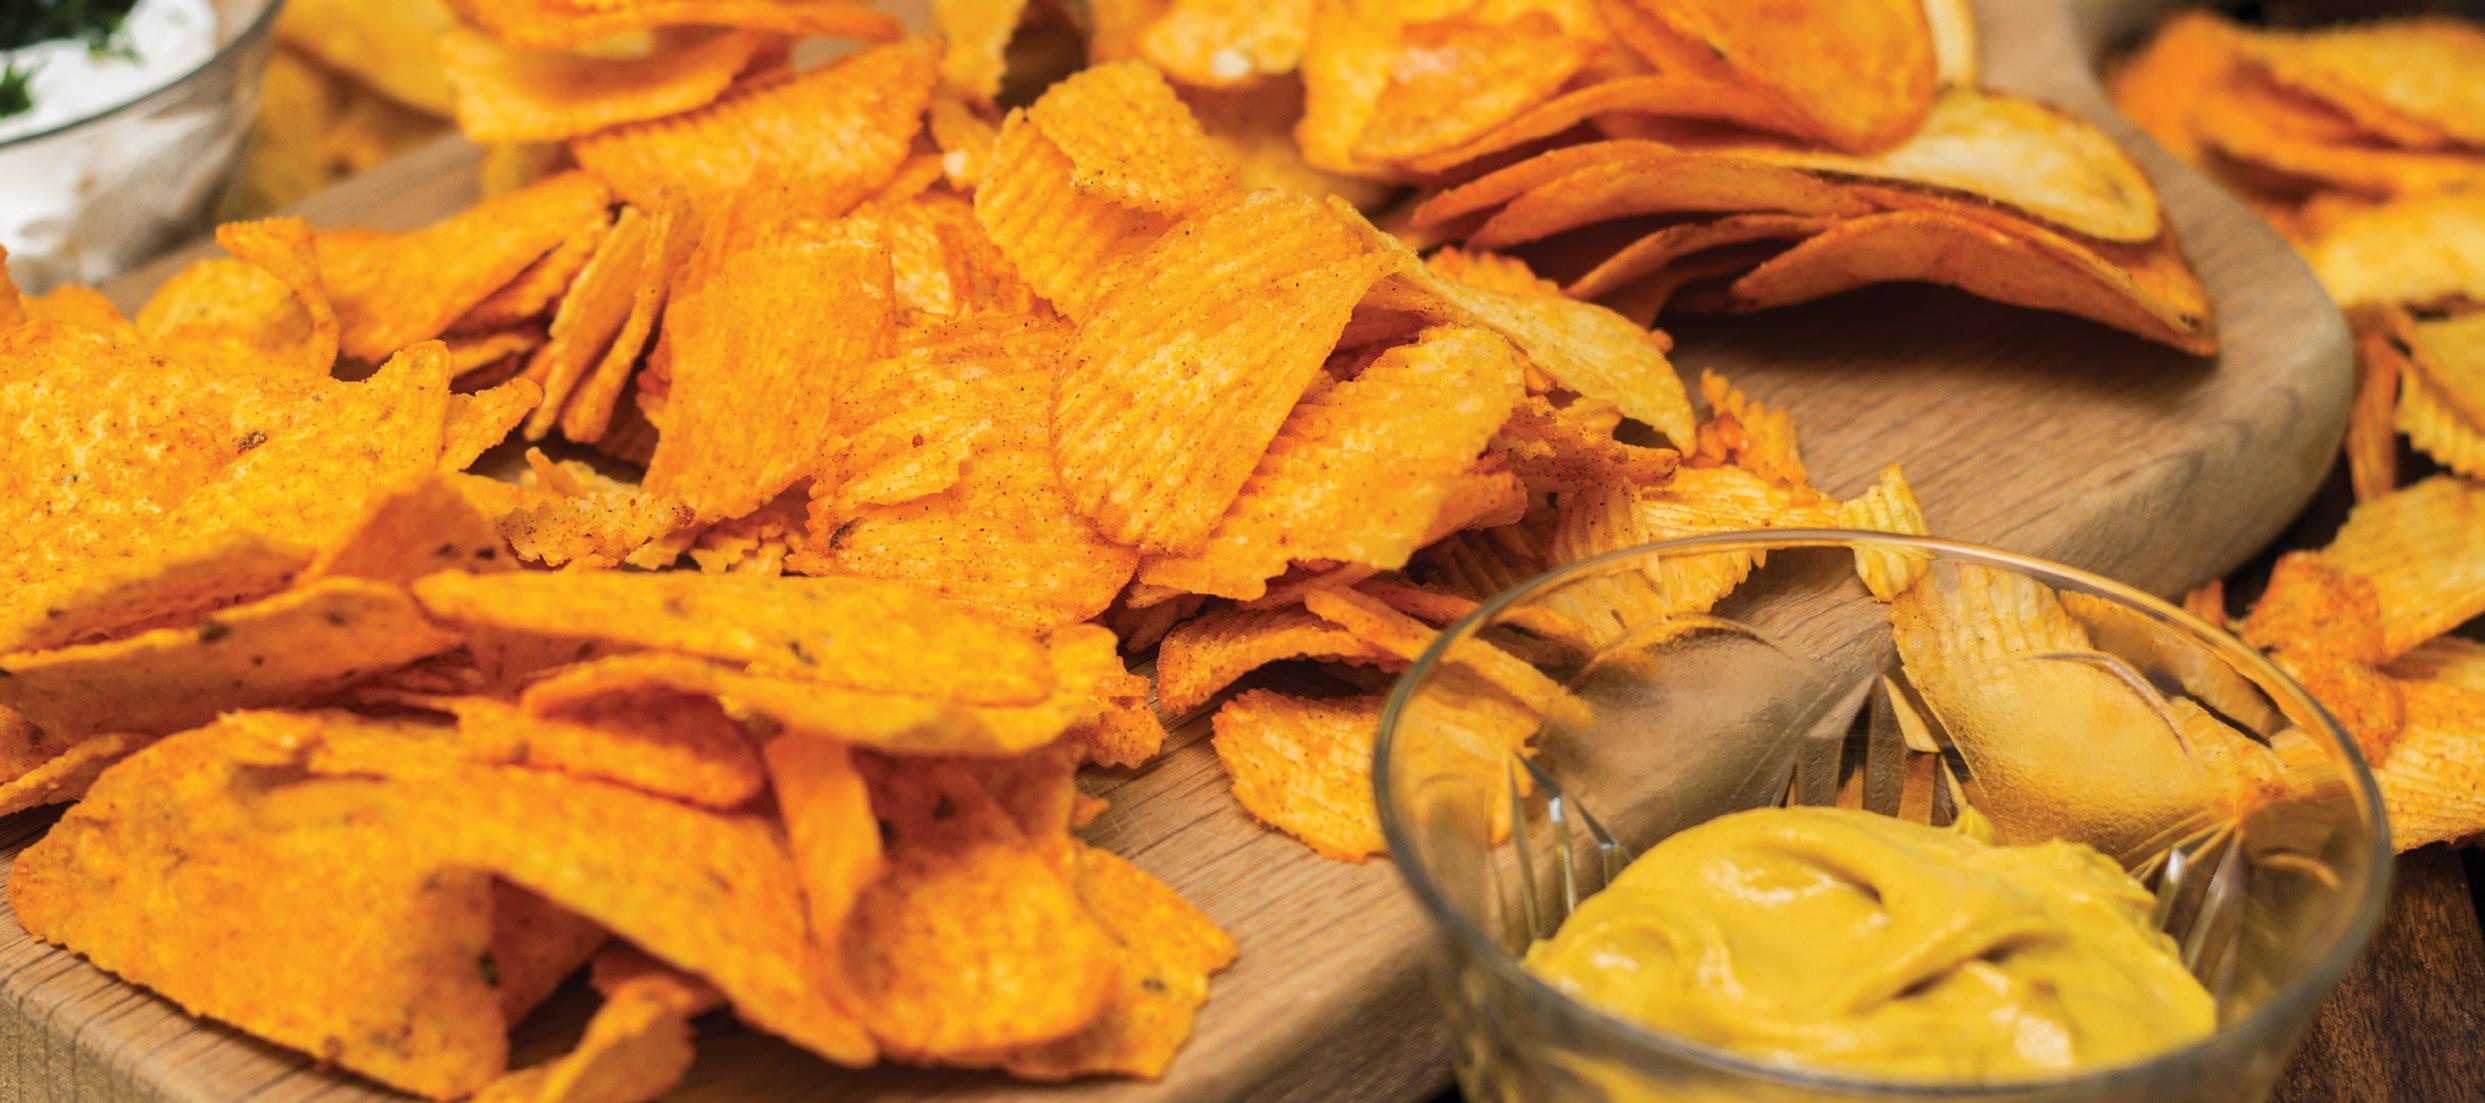
South Africa’s savoury market is moving boldly away from the bland. Layered flavours, global inspiration and fermentation-derived ingredients are redefining how snacks, marinades and seasonings excite consumers.
South Africa’s savoury market offers a powerful lens into how bold flavour, global inspiration and indulgent taste cues continue to shape consumer choice. Recent innovation across snacks, marinades and seasonings shows a clear move away from neutrality and towards deeper, more expressive flavour experiences, where taste delivery is as important as convenience and familiarity.
Drawing inspiration from these trends, flavour design today is increasingly about layering intensity, authenticity and culinary character — an area where umami, kokumi and fermentation-derived flavour ingredients play a central role. From everyday snacks to elevated experiences, flavour innovation has become a key driver of value creation in South Africa’s snack landscape. Brands are prioritising new flavour variations over entirely new products, reflecting strong consumer appetite for discovering new tastes within familiar formats. Plain or unflavoured snacks are steadily losing ground, while flavour-forward propositions continue to expand.
Among savoury snacks, several flavour families show particularly strong momentum: vegetable- and allium-led profiles such as roasted onion, red onion and bell pepper; heat-forward and sweet-heat combinations including chipotle chilli and hot honey; tangy and pickled notes that deliver brightness and contrast; umami-rich and chef-inspired cues such as mushroom, pesto and Mediterranean flavours; meaty, smoky and BBQ-style profiles associated with indulgence and
"Bold flavour directions, backed by fermentation-derived taste tools — that is how inspiration becomes a concept that scales."
comfort; and premium seafood inspirations illustrated by prawn cocktail and lobsterinspired launches. Together, these trends highlight a clear demand for flavours that feel richer, more rounded and more culinary — even in everyday snack formats.
The same flavour logic extends naturally into marinades and seasoning systems, where innovation increasingly focuses on quick, low-effort solutions combined with bold global flavour cues. South African launches continue to draw inspiration from Mediterranean, Cajun, Buffalo and Spanish cuisines, alongside strong momentum for smoky BBQ profiles, chilli-led concepts and sweet-savoury combinations. Across both snacks and marinades, the common denominator remains consistent: taste intensity, depth and balance are essential to create excitement, differentiation and repeat purchase.
As flavour profiles become more layered and expressive, umami plays a foundational role in supporting savoury impact and coherence. Umami-rich ingredients help create roundness, continuity and lingering taste, particularly valuable in vegetable-
forward, plant-based or globally inspired recipes. Yeast extracts, obtained through fermentation, offer a natural source of amino acids, peptides and nucleotides that contribute clean savoury taste while supporting simpler, more recognisable ingredient lists. In snack seasonings, they act as efficient flavour carriers, anchoring bold top notes such as chilli heat, smoke or herbs into a cohesive savoury base. In marinades, they provide fast flavour release and consistency, aligning well with conveniencedriven cooking habits.
Solutions such as High-Lyfe® 530 A, produced by Lallemand Bio-Ingredients, offer a clean, savoury umami profile that integrates seamlessly into snacks, seasonings and marinades. For formulators seeking both flavour efficiency and simplicity, Whole-Lyfe® 985 A provides a ready-to-use yeast autolysate that combines umami impact with toasted savoury notes. Beyond flavour alone, Whole-Lyfe® 985 A retains yeast cell-wall components, which naturally contribute to a fatty and creamy mouthfeel perception and can support emulsification and flavour carryover — particularly relevant in marinades, coatings and rich seasoning systems. This multifunctional behaviour helps deliver indulgence and texture while maintaining a natural, clean-label positioning.
Within meaty and BBQ-style flavour directions, fermentation-based ingredients play an especially important role. Chicken remains one of the most versatile and widely appreciated taste cues across the South

















African market, translating easily across snacks, coatings and marinades. Clean, savoury chicken flavour systems such as Savor-Lyfe® CI (Chicken Intense) help deliver roasted and cooked chicken character with depth and roundness, reinforcing comfort and familiarity while allowing space for spices, herbs or heat to shine.
Beef-inspired profiles remain equally relevant in indulgent snack seasonings and BBQ marinades, where savoury richness and roasted notes are key drivers of satisfaction. Solutions such as Savor-Lyfe® BEC, delivering roasted beef character, help build meaty intensity and mouth-coating savouriness without overpowering the overall flavour profile.
Smoky and BBQ-style flavours continue to rank among the most indulgent and emotionally resonant taste cues. Bacon-inspired flavour directions, in particular, play a strong role in reinforcing smoke, fat perception and grilled character across snacks and seasoning blends. Smoked inactive yeast such as Bakon® HFBN, combined with meat lines such as SavorLyfe® PH and PR, allow formulators to create BBQ profiles that feel authentic, rounded and lingering — supporting indulgence while maintaining formulation flexibility and cleanlabel positioning, even in vegan-suitable forms.
Kokumi: Adding richness without changing the flavour - Beyond umami, kokumi characteristics are increasingly relevant as consumers gravitate towards flavours perceived as rich, indulgent and wellrounded. Kokumi contributes to enhanced mouthfeel, flavour continuity and a lingering savoury impression, all without changing
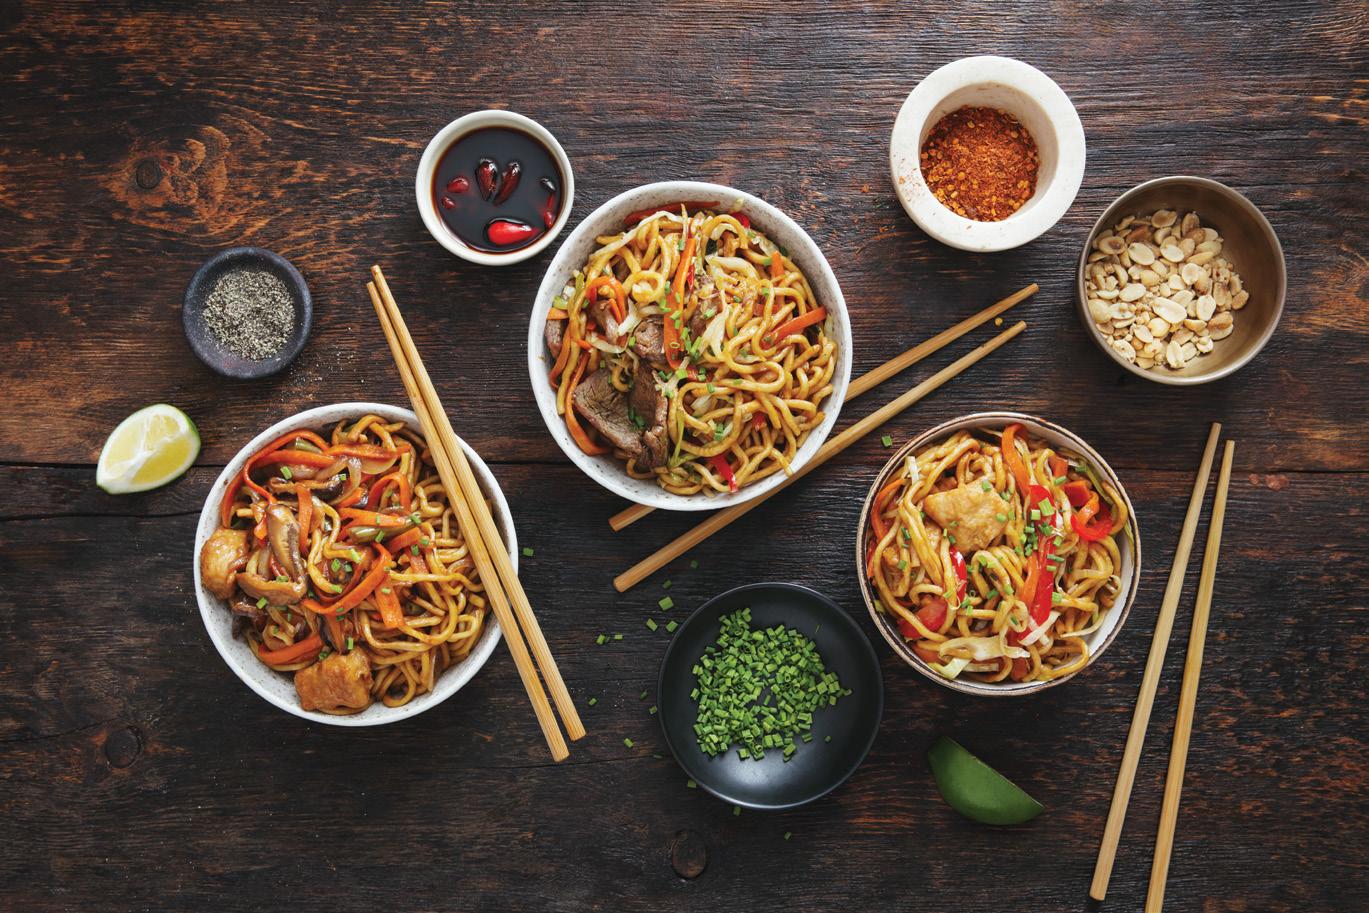
the core flavour itself. Ingredients such as High-Lyfe® 605 A, a yeast extract rich in glutathione and cysteine peptides, have been specifically developed to deliver this effect in savoury applications.
In indulgent snack seasonings — such as smoky BBQ blends — or in creamy and oil-based marinades, kokumi-active yeast extracts help reinforce perceptions of balance, richness and complexity, attributes closely associated with quality and indulgence in the South African market. Premium seafood: Fine-dining flavours in everyday formats - Another flavour space gaining visibility is premium seafood inspiration, where everyday products borrow cues from restaurant-style and fine-dining flavours. Crustacean-inspired profiles, including lobster and prawn seasonings, bring intense umami, subtle sweetness and refined savoury character. Supported by umami- and kokumi-rich yeast ingredients,
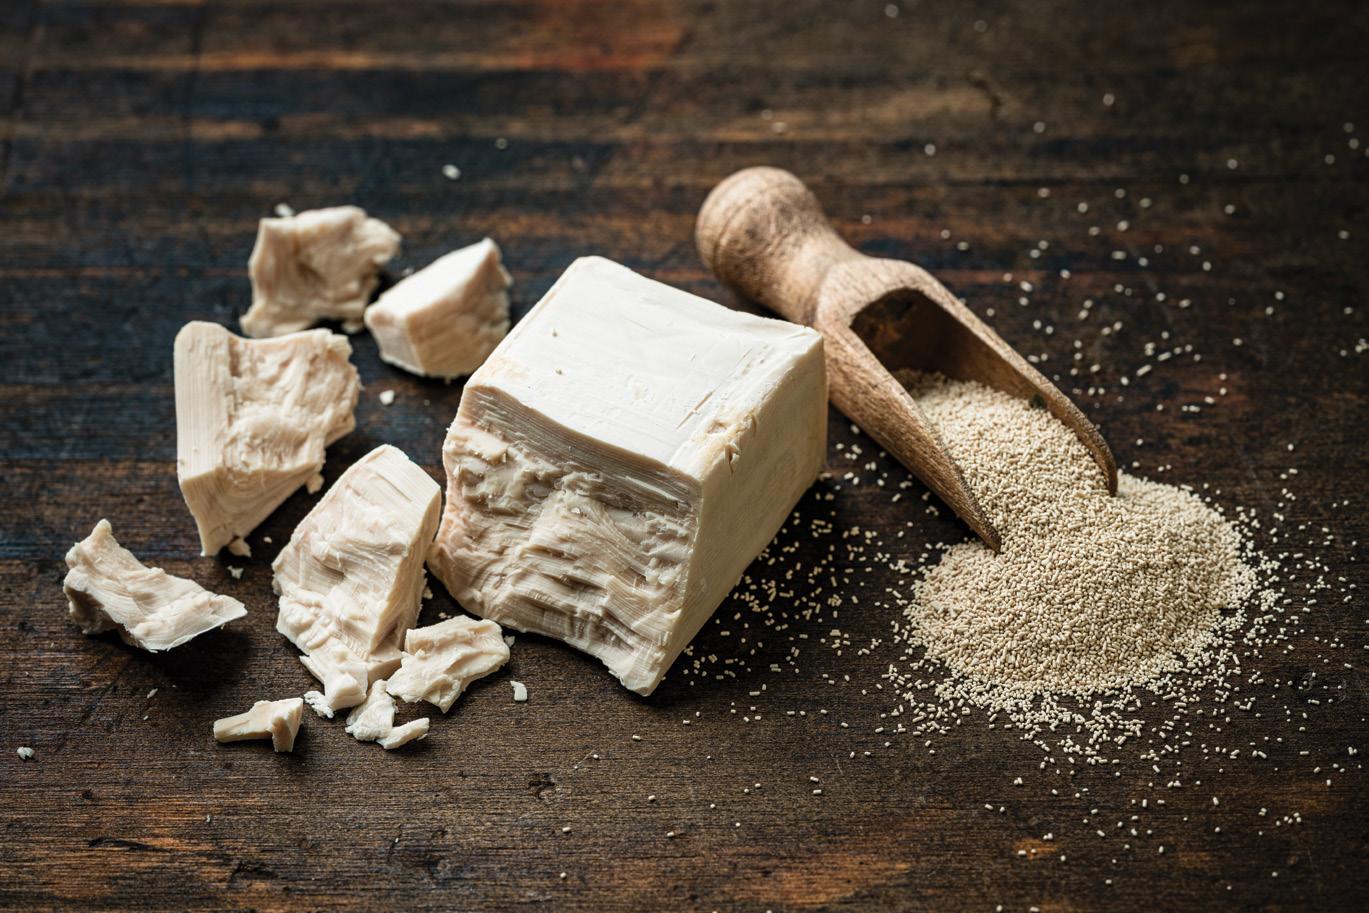
these flavours can be adapted across snacks, coatings, seasonings and marinades to deliver impact without overwhelming the finished product.
Ultimately, South Africa’s flavour trends point towards a future where boldness is balanced with structure, and innovation builds on strong savoury foundations rather than novelty alone. By combining clear flavour directions — vegetable-led savoury, global heat, indulgent meat and BBQ cues, and premium seafood — with fermentationderived taste tools such as umami and kokumi yeast ingredients, food makers can translate inspiration into robust, scalable concepts. The result is flavours that feel richer, more indulgent and more memorable, while remaining adaptable across formats and markets.
As Lallemand Bio-Ingredients states, yeast is the bridge to the future of food, enabling the industry to meet evolving expectations for taste, simplicity, safety and sustainability.
Yeast extracts produced through fermentation are a natural source of amino acids, peptides and nucleotides — the building blocks of clean, satisfying savoury taste — while supporting simpler, more recognisable ingredient lists.
For more than two decades, NuBerry Fruits has been quietly doing the work that matters most in food manufacturing — delivering consistent quality, real flexibility and the kind of technical reliability that keeps dairy and beverage producers coming back.
NuBerry Fruits was founded in 2005 with a clear sense of purpose: to give South African dairy and drinks manufacturers access to fruit preparations, syrups and flavour systems that are genuinely tailored to their needs. Not offthe-shelf. Not a catalogue pick. Products developed in close collaboration with the people who are going to use them.
More than twenty years on, that founding logic still drives everything the company does. From the Cape Town facility — designed with dedicated receiving, manufacturing and dispatch areas — NuBerry operates with the kind of precision that food safety-conscious producers demand. What has changed is the scope. The product range has grown considerably, the production capabilities have deepened, and the customer base now extends well beyond South Africa’s borders.
The core of NuBerry’s business remains what it has always
been: customer-specific, flavoured and concentrated fruit and syrup preparations for yoghurt, smoothie and other dairy applications. These are not generic formulations. Each preparation is developed to spec, tested thoroughly, and adjusted until it performs exactly as required in the end product.
The range covers fruited yoghurt preparations, smooth yoghurt syrup preparations, smoothie preparations, flavour and colour compound combinations, juice and nectar concentrates, milk blend concentrates, and liquid or powder formulations for dairybased drinks. It is a broad offering, but one that is held together by a consistent thread — the ability to deliver precisely what a specific application demands, at the quality level the market expects.
One of the more practical differentiators NuBerry brings to the table is its production flexibility. Batch sizes range from 250 kg to 5 tonnes, with customisable filling, weighing and
packaging options that can be matched to individual customer requirements. For manufacturers dealing with seasonal demand swings or product line changes, that kind of adaptability is not a nice-to-have — it is operationally essential.
It also speaks to NuBerry’s positioning in the market: a company that is agile enough to respond when circumstances shift but established enough to sustain consistent output and service delivery over time. There is a particular kind of credibility that comes from being in business for nearly two decades without cutting corners on quality, and NuBerry has earned it.
FSSC 22000 certification sits at the centre of NuBerry’s quality framework. It is not a badge on a website — it is the result of rigorous, ongoing compliance with globally recognised food safety management standards. Every batch produced at the Cape Town facility undergoes thorough testing to ensure quality, safety and compliance. Raw materials are sourced exclusively from audited local and international suppliers, with each incoming delivery subject to inspection before it enters the production line.
Certificates of analysis accompany every delivery, giving customers complete visibility into what they are receiving. In an industry where a single out-of-spec batch
can derail a production schedule, that level of traceability and documentation carries real weight. It is the kind of quality assurance infrastructure that leading manufacturers rely on when the stakes are high.
NuBerry’s approach to product development is grounded in what customers are asking for, combined with a clear-eyed view of where the market is heading. Over recent years, the company has expanded deliberately into areas that make full use of its existing formulation expertise — sugar-replacement syrups, milk-fat replacers, powder blends, and concentrates and colour/flavour compounds for the dairy, juice and soft drink industries.
These are not diversification moves made for the sake of it. Each extension of the portfolio reflects a genuine gap that NuBerry’s technical team identified and addressed through its in-house development capability. The stateof-the-art facility supports both new product development and the continuous refinement of existing formulations — whether that means responding to a
“Small enough to move fast. Large enough to deliver every time.”
specific customer brief or getting ahead of a category shift before it peaks.
The distinction NuBerry draws between being a supplier and being a partner is more than marketing language. It shows up in the day-to-day: in the responsiveness of the team, in the willingness to develop and iterate until a formulation is right, and in the operational discipline that ensures lead times are met consistently. The company’s values — service excellence, quality, integrity, efficiency, and innovation — are
NuBerry Fruits can scale a single production batch from 250 kg all the way up to 5 tonnes — adapting to your volume, not the other way around.
not aspirational statements. They are the operating principles that have kept NuBerry relevant and growing for nearly two decades. For dairy and beverage manufacturers looking for a South African ingredients partner with genuine technical depth, a proven quality record and the production agility to handle what the market throws at them, NuBerry Fruits makes a compelling case. Not because it says all the right things — but because the track record backs it up. To explore NuBerry Fruits’ full product range or discuss a development brief, contact the team directly.
Every single batch produced at NuBerry Fruits undergoes thorough testing to ensure quality, safety and compliance — before it ever leaves the Cape Town facility.
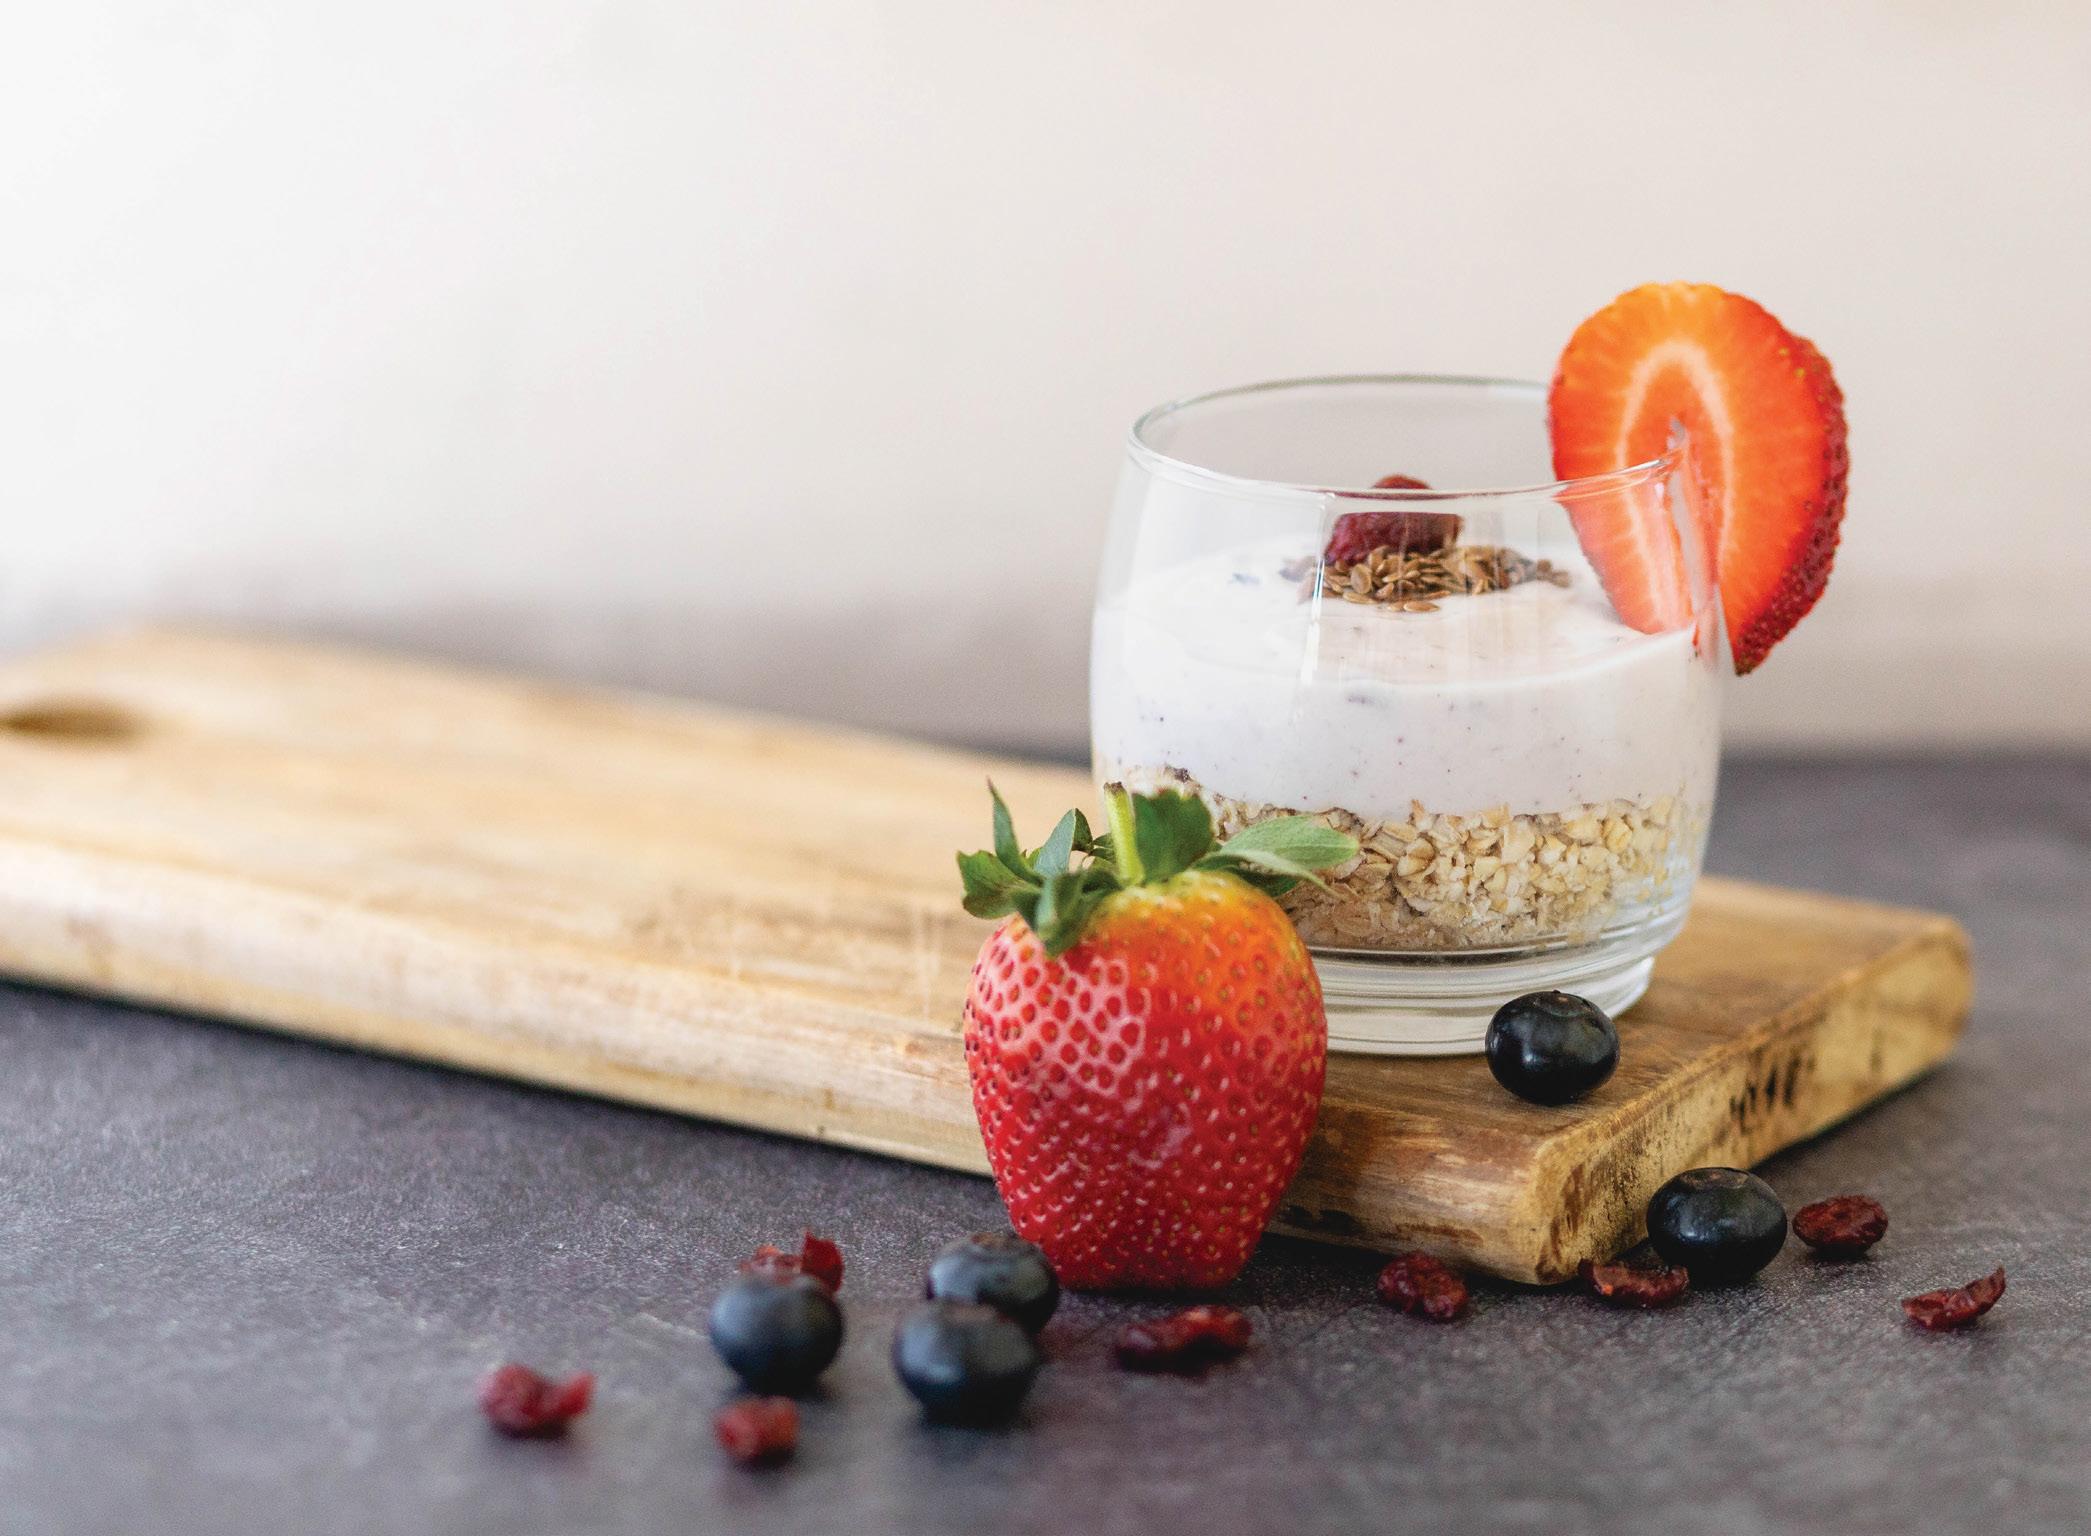
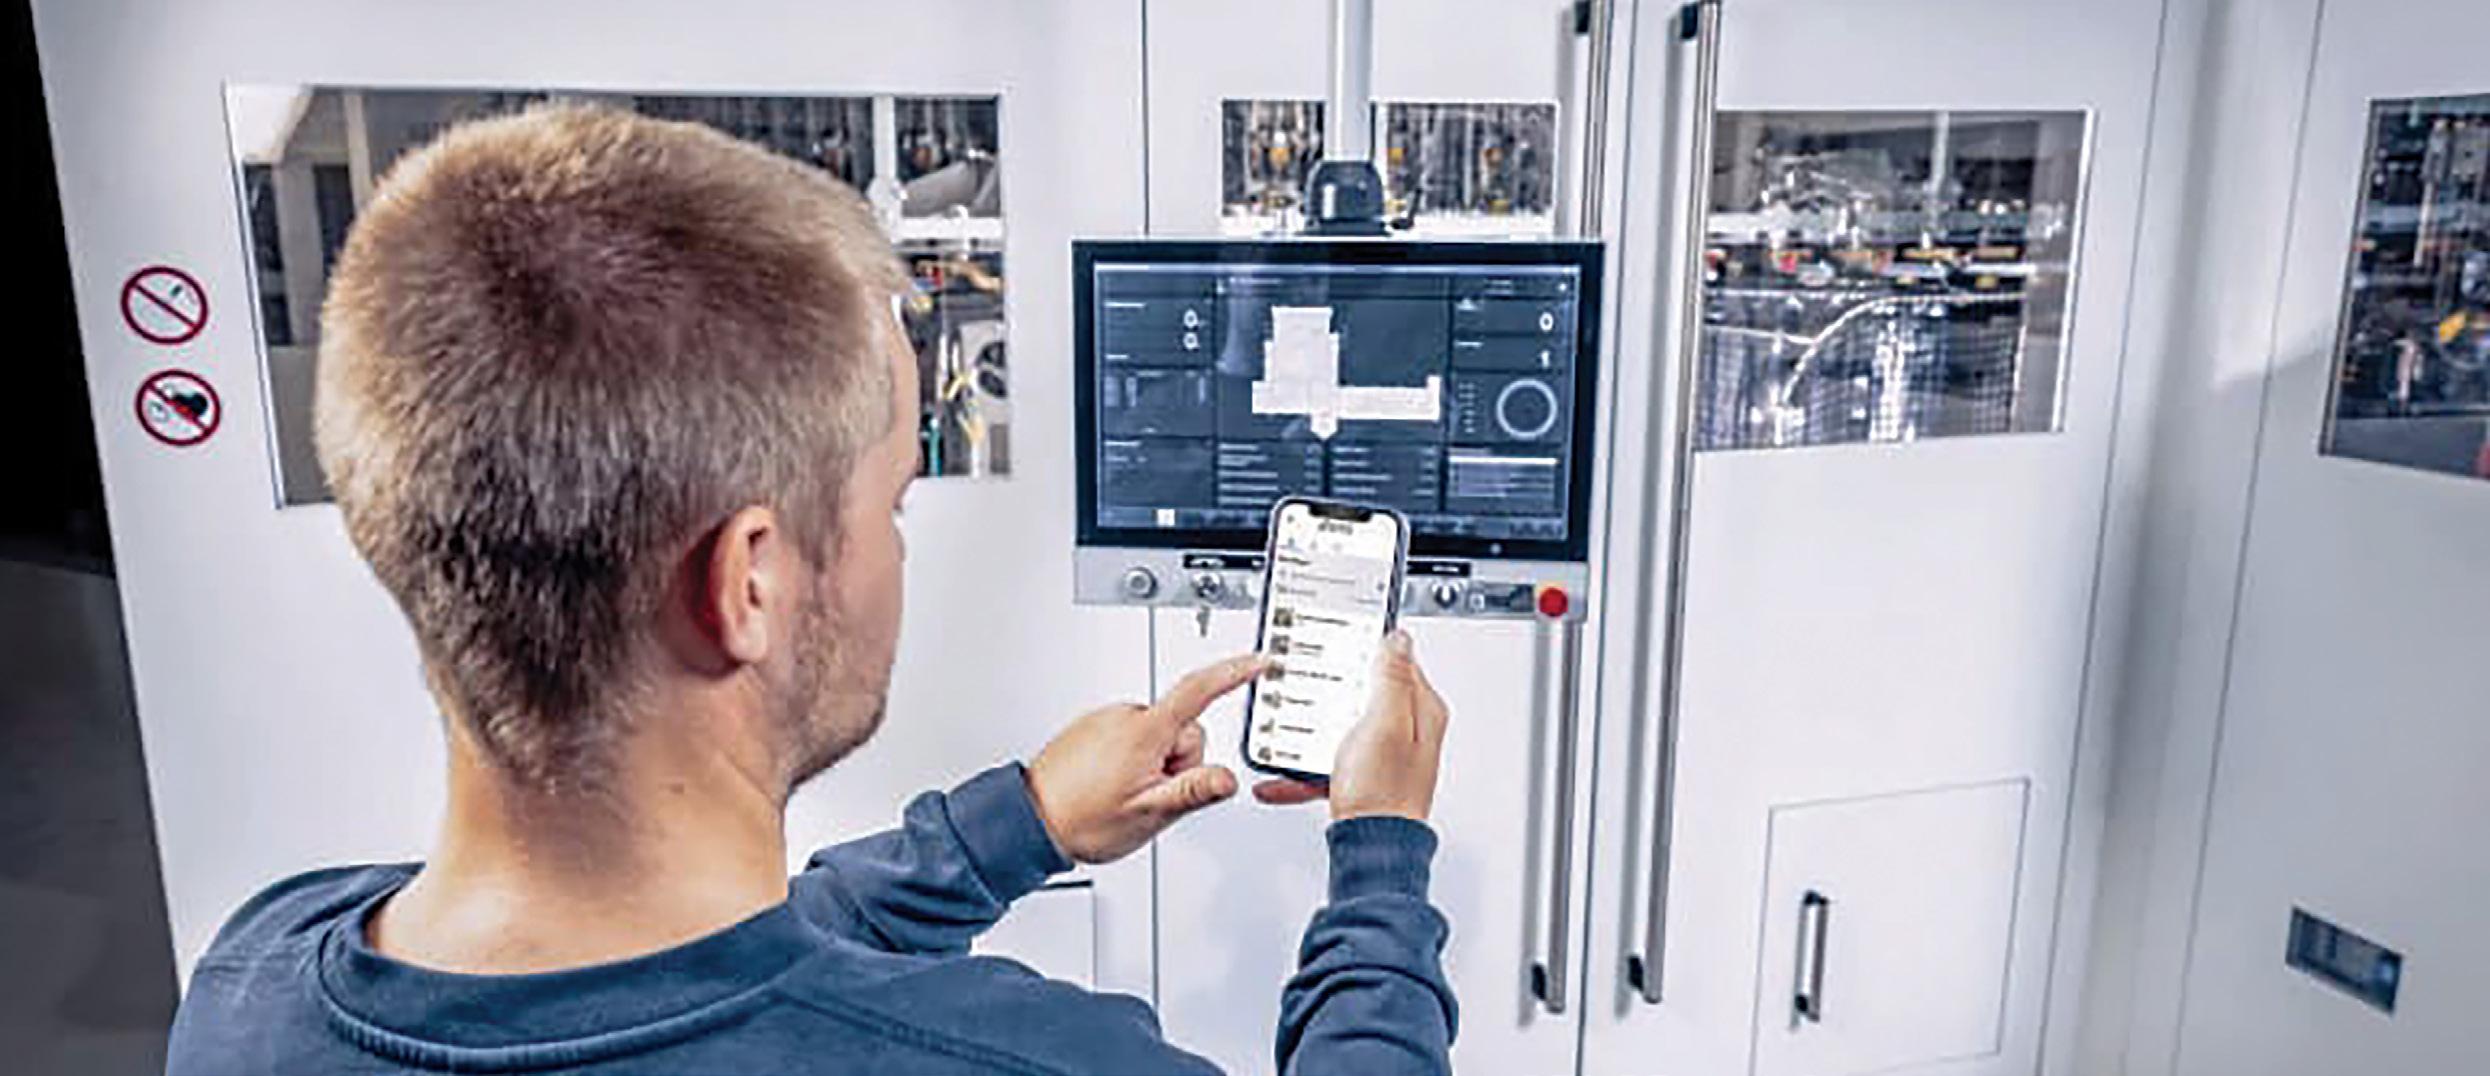
KHS Group's upgraded ConnectApp Guide replaces rigid maintenance schedules with intelligent, usage-driven task management — cutting downtime, reducing costs and putting real-time machine data directly in operators' hands.
With immediate effect, the KHS Group is giving beverage producers more help with the servicing of their machines. Thanks to the addition of various new functions, KHS ConnectApp Guide now makes maintenance management even more efficient: by integrating bills of materials and introducing dynamic, usage-dependent maintenance intervals, the application is better attuned to the actual level of system wear. This saves time, conserves resources and optimises spare-parts stockkeeping.
Since its launch in March 2024, the standalone app and intuitive digital assistant KHS ConnectApp Guide has brought valuable maintenance expertise straight to the shop floor. The system specifically digitalises daily CILT tasks — namely essential routines in cleaning, inspection, lubrication and tightening of components. In place of the former Excel lists or PDFs, the app now proactively reminds personnel of all due routines, prompting them through the processes like a task manager, considerably helping to maintain line availability in the long term.
The further development of KHS ConnectApp Guide has yielded key added value: a reduction in the total cost of ownership (TCO). Thanks to less downtime, on-demand maintenance intervals and more efficient processes, users benefit from sustainable savings in ongoing operation. This new digital feature is a prime element in KHS' holistic line concept. With processes precisely co-ordinated with one another, the turnkey supplier from Dortmund, Germany, gives its customers high system availability
"Beverage producers reported training periods being shortened by up to 80%."
plus optimised overall costs throughout the line's entire life cycle.
"The app's intuitive operation received very positive ratings in our pilot projects," says Deniz Ulutürk, digital products manager at KHS. "Beverage producers reported training periods being shortened by up to 80%."
One major improvement in the latest version of the app is that task control has been radically extended. Until recently, the software managed maintenance tasks according to time, scheduling work at fixed intervals — two days or two weeks, for example — regardless of whether the machine was running at full capacity or was at a standstill. With the app's new dynamic task function, maintenance is now accurately based on the actual number of operating hours.
"Time-based planning has established itself as standard, yet demand-based management considerably further optimises this process," explains Ulutürk. "If a machine is down for a week, components that are only subject to wear during operation don't need to be inspected unnecessarily." Dynamic tasks therefore both protect the system and conserve resources.
This is technically facilitated by the seam -
less interaction of the app's components.
New KHS systems now leave the factory equipped with an edge device — a compact industrial computer that logs production data directly on the machine and sends it through the secure KHS ConnectApp Access cloud link to the system. KHS ConnectApp Guide then analyses this data in real time. When a defined operating-hour threshold is reached, the relevant maintenance task automatically appears on the employee's mobile device and the production manager web platform.
This ensures that maintenance steps can be precisely co-ordinated based on demand throughout the entire line, ensuring no link in the production chain is overlooked. Customers can also independently add third-party machines and equipment to their system.
Task precision is supplemented by a further new feature: complete bills of materials directly uploaded onto the machine at the factory. With this, KHS links digital task management to the technical 'memory' of the respective machine. Customers receive their lines pre-configured with all spare parts and their ID numbers.
"By including bills of materials, we're saving customers from having to research," Ulutürk says. "With BOMs, employees have access to full, up-to-date maintenance information at all times. This means fewer queries and a consistently high quality of execution."
In today’s world, where the safety and quality of food products are non-negotiable, laboratories providing testing services play a pivotal role in protecting public health. One such institution leading the way in reliable testing services is MLS Laboratories, a renowned name in the field of laboratory testing for the past 30 years.
By staying ahead of industry trends, MLS ensures that its services are adaptable to the evolving needs of its clients. Whether it’s testing for emerging pathogens or ensuring that
new, innovative products meet safety requirements, the lab’s capacity for innovation makes it a key partner in industries where precision and foresight are paramount.
MLS Laboratories offers a wide range of testing services, including food safety testing, nutritional testing, environmental testing, and the testing of products for harmful contaminants such as heavy metals, pesticides, and microbiological agents. The laboratory ensures that results are accurate, reproducible, and scientifically sound. This commitment
to quality is not just about meeting regulatory standards—it’s about safeguarding the well-being of individuals, communities, and ecosystems at large.
NATIONWIDE EXCELLENCE
MLS National Laboratory Services and Supplies is a fully ISO 17025 laboratory based in Midrand, KZN and Cape Town, with a significant footprint across South Africa.
– www.mlslabs.co.za
Sustainability has become a critical component of operational resilience in the food industry. Forward-thinking organisations are embedding sustainable practices to reduce risk, ensure compliance and create long-term value.
sourcing, supplier diversification and traceability reduce exposure to disruptions and strengthen continuity. KEY RISK AREAS ADDRESSED
SUPPLY CHAIN STABILITY
RESOURCE EFFICIENCY Efficient use of water, energy and raw materials reduces operational risk and supports long-term cost management.
Proactive environmental and governance systems help organisations meet evolving regulations and reduce
Inline pump filling equipment
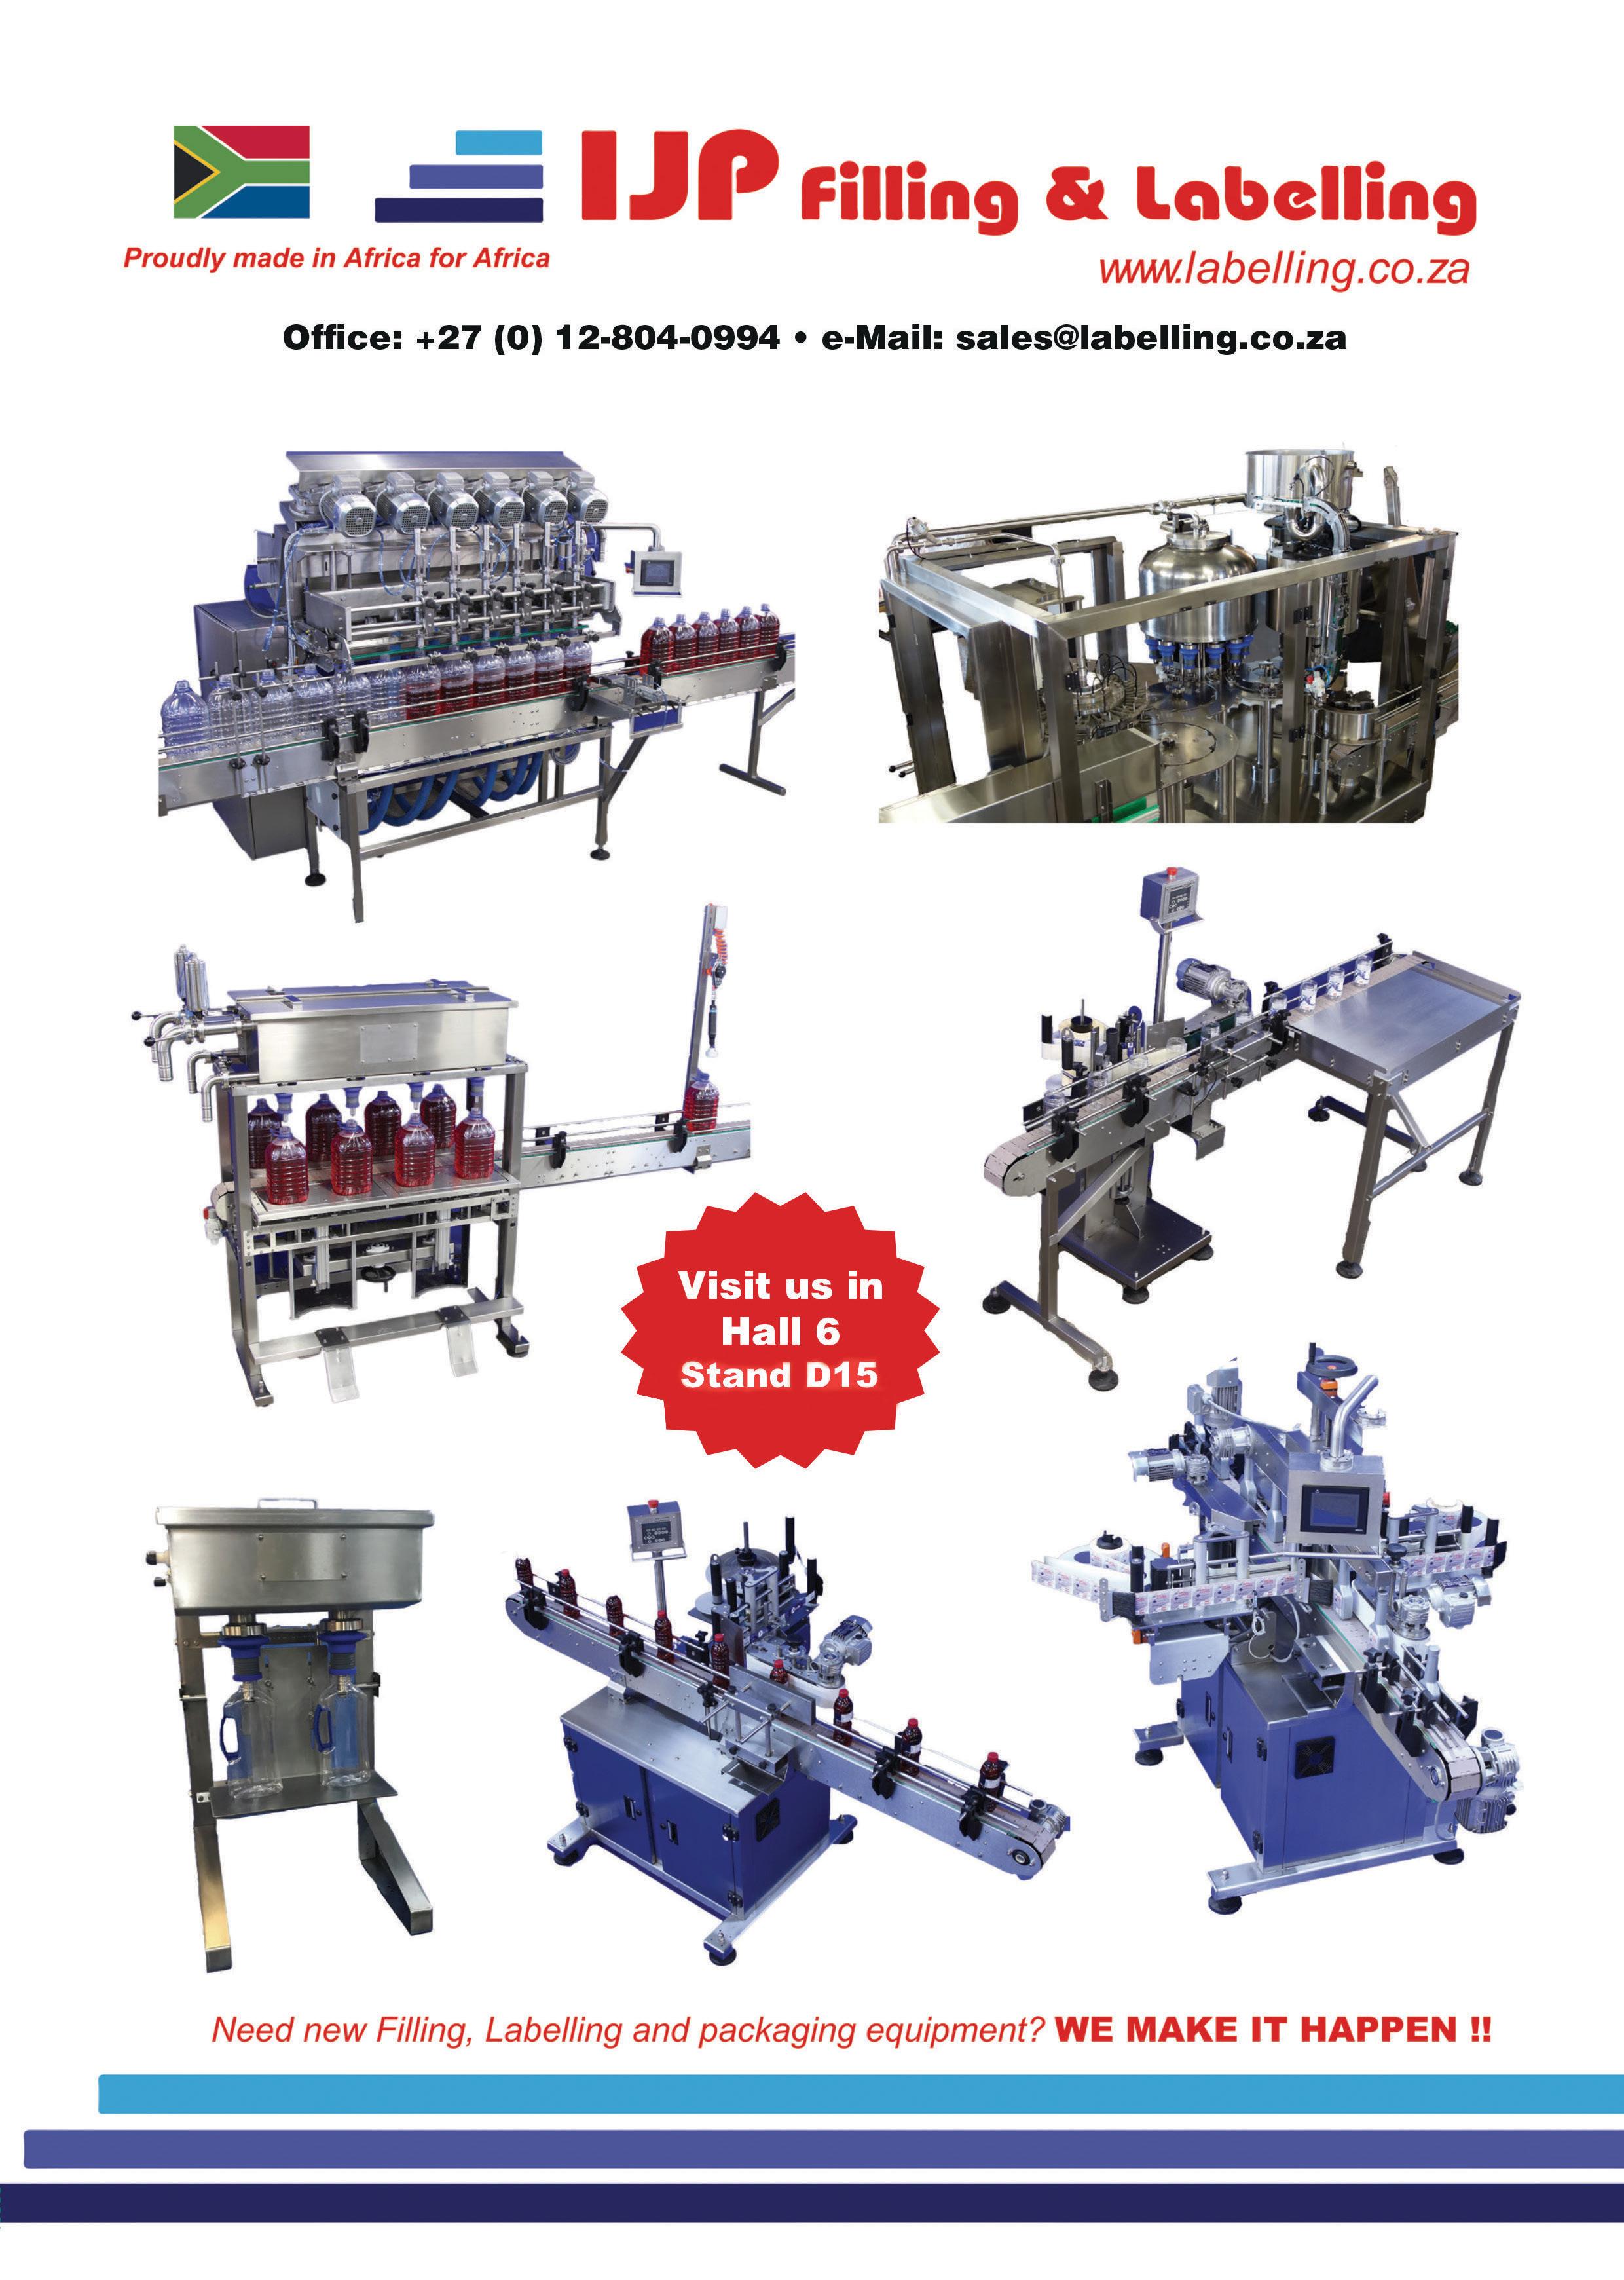
equipment
Round bottle labelling
Gravity filling equipment
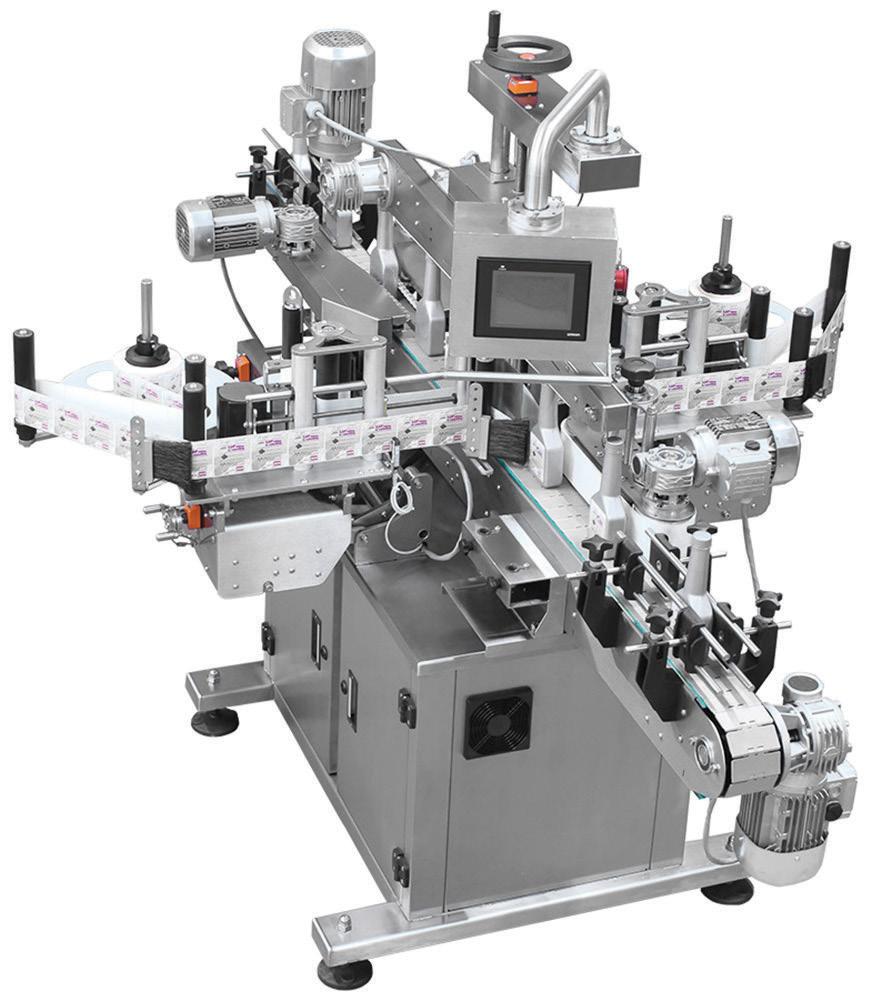
Entry level filling equipment
Front and back labelling
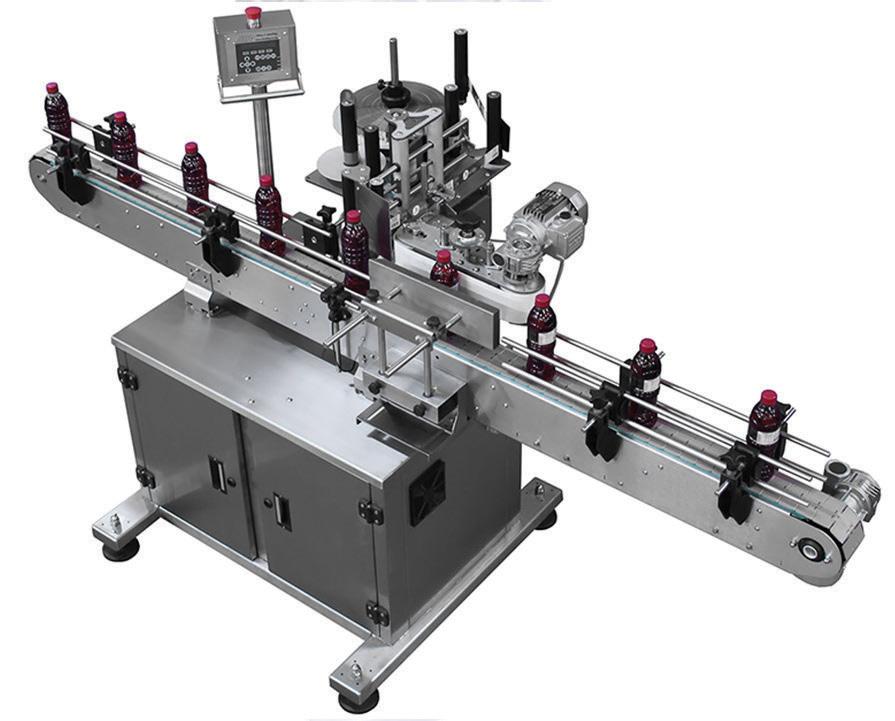
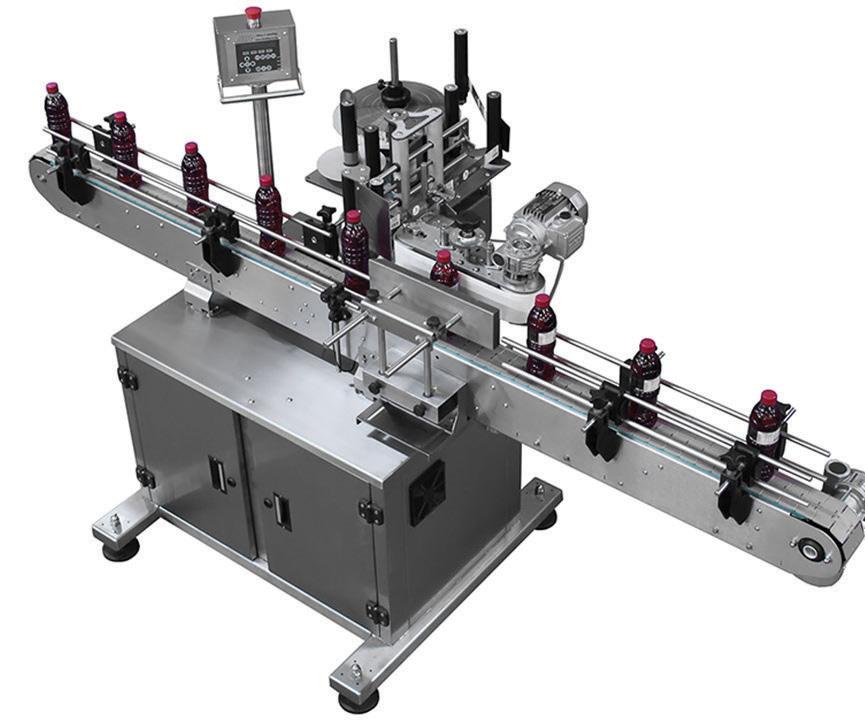
Pharmaceutical labelling & coding