Leading
Horizontal Pump Manufacturers for Industrial Fluid Handling
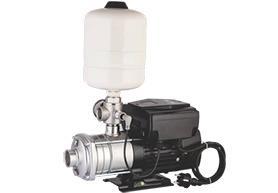
Industrial fluid handling plays a crucial role in keeping manufacturing, processing, and utility systems running smoothly. From water transfer to chemical processing and wastewater treatment, reliable pumping systems ensure uninterrupted operations and improved productivity. Among the many solutions available, horizontal pump systems are widely preferred for their stability, ease of maintenance, and efficiency in handling large volumes of fluids.
In today’s competitive market, industries depend heavily on trusted Horizontal Pump Manufacturers who can deliver durable and high-performance equipment tailored to specific operational needs. These manufacturers focus on designing pumps that can withstand harsh working conditions while maintaining consistent flow rates and energy efficiency.
Importance of Reliable Pumping Systems in Industries
Every industrial process depends on the smooth movement of liquids. Any disruption can lead to production delays, equipment damage, and increased operational costs.
This is why industries invest in high-quality pumping systems designed for continuous performance.
Modern facilities often rely on solutions developed by experienced Horizontal Pump Manufacturers to ensure operational stability. These systems are engineered to handle a wide range of fluids, including clean water, chemicals, and abrasive liquids. Their horizontal design provides better balance, reduced vibration, and easier maintenance access, making them suitable for long-term industrial use.
Role of Horizontal Pumps in Fluid Handling
Horizontal pumps are widely used across industries such as chemical processing, power generation, pharmaceuticals, food processing, and wastewater treatment. Their ability to handle high flow rates and maintain consistent pressure makes them a preferred choice for large-scale operations.
Many industries also depend on Chemical Pump systems for handling corrosive and hazardous liquids. These pumps are specially designed with corrosion-resistant materials to ensure safety and durability in challenging environments. When combined with horizontal pump systems, they create a more efficient and reliable fluid handling setup.
Growing Demand for Advanced Pump Technologies
With increasing industrialization, the demand for efficient pumping solutions has grown significantly. Companies are looking for equipment that not only improves productivity but also reduces energy consumption and maintenance costs.
Leading Horizontal Pump Manufacturers are continuously innovating to meet these demands. They are integrating advanced engineering techniques, high-efficiency motors, and improved sealing technologies to enhance pump performance. These improvements help industries achieve better operational control and lower downtime.
In addition, the rise of automation has encouraged manufacturers to develop smart pumping systems that allow real-time monitoring and predictive maintenance. This ensures early detection of issues and prevents unexpected breakdowns.
Industrial Applications of Pump Systems
Horizontal pumps are used in a wide variety of applications, making them one of the most versatile pumping solutions available today. Some common applications include:
Water supply and distribution systems
Chemical processing plants
Cooling and heating systems
Wastewater treatment facilities
Oil and gas industries
Food and beverage processing
In chemical industries, Chemical Pump systems play a vital role in safely transferring reactive and corrosive liquids. Their specialized construction ensures safe handling and long service life even in demanding environments.
Similarly, Centrifugal Pump Manufacturers provide solutions that are widely used for transferring fluids with high efficiency. These pumps are known for their simple design, low maintenance, and ability to handle large volumes of liquid, making them suitable for multiple industrial sectors.
Key Features of Modern Pumping Solutions
Modern pumping systems are designed with advanced features to improve reliability and efficiency. Some important features include:
High hydraulic efficiency for reduced energy usage
Strong and durable construction materials
Corrosion and abrasion resistance
Easy installation and maintenance
Stable performance under varying loads
Low vibration and noise levels
These features ensure that industries can operate smoothly without frequent interruptions or costly repairs.
Importance of Choosing the Right Manufacturer
Selecting the right supplier is essential for achieving long-term performance and reliability. Experienced Horizontal Pump Manufacturers focus on quality engineering, strict testing standards, and customer-specific solutions.
Industries often evaluate manufacturers based on product durability, energy efficiency, after-sales support, and customization options. A reliable manufacturer ensures that the pumping system is designed according to operational requirements, which helps improve efficiency and reduce lifecycle costs.
Expanding Role of Pump Engineering in Industry
As industries evolve, pumping technology continues to advance. Manufacturers are now focusing on energy-efficient designs and environmentally friendly solutions. Improved impeller designs, optimized flow paths, and advanced materials are helping reduce energy consumption while increasing output.
The role of Centrifugal Pump Manufacturers has also expanded significantly in this space. Their innovations contribute to more efficient fluid transfer systems that support both small-scale and large-scale industrial applications.
At the same time, specialized Chemical Pump systems are being designed to meet strict safety standards, ensuring safe handling of hazardous materials in chemical plants and laboratories.
Future of Industrial Pumping Solutions
The future of industrial pumping lies in smart technology and sustainability. Advanced pump technologies equipped with smart sensors, continuous performance tracking, and predictive servicing capabilities are helping industries optimize fluid movement processes. These innovations enable faster issue detection, minimize unplanned downtime, improve operational efficiency, and support better maintenance planning for long-term system reliability. These innovations help reduce downtime, improve efficiency, and extend equipment lifespan.
Manufacturers are also focusing on eco-friendly solutions that minimize energy usage and environmental impact. This shift is encouraging industries to adopt more efficient pumping systems that align with global sustainability goals.
Conclusion
Efficient fluid handling is essential for industrial success, and selecting the right pumping equipment plays a vital role in achieving operational excellence. High-quality systems developed by trusted Horizontal Pump Manufacturers ensure smooth performance, energy efficiency, and long-term reliability across various applications.
Whether it is chemical processing, water treatment, or industrial manufacturing, choosing the right pumping solution can significantly improve productivity and reduce operational costs. Advanced Centrifugal Pump Manufacturers and specialized Chemical Pump systems further enhance industrial capabilities by offering tailored solutions for different fluid handling needs.
For industries looking for reliable and high-performance pumping solutions, JEE Pumps offers advanced engineering, durable designs, and customer-focused services to meet modern industrial demands. Get in touch with JEE Pumps today to explore efficient and long-lasting pumping solutions designed for your business growth and operational success.
Contact Details
Website: www.jeepumps.com
Contact No: +91-9687650618
Contact Mail: info@jeepumps.com