INDUSTRIAL NETWORKS: Selecting components that make the grade. p.24
INTERNET OF THINGS: Manufacturers who embrace IoT are leading the digital transformation. p.23
MACHINE SAFETY: Ensuring safe operations with collaborative robots. p.14
AutomationMag.com
Your resource for Canada’s industrial automation news
THE SLOW
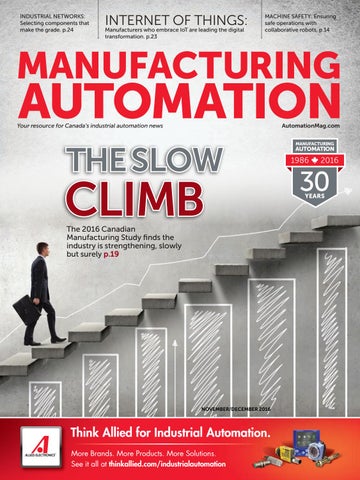
CLIMB The 2016 Canadian Manufacturing Study finds the industry is strengthening, slowly but surely p.19
NOVEMBER/DECEMBER 2016
Think Allied for Industrial Automation. More Brands. More Products. More Solutions. See it all at thinkallied.com/industrialautomation
One PLC...endless possibilities! CPU with USB
5
COMM PORTS
built in!
Modbus®
RS-232
2016 RS-485 FINALISTS
ETHERNET
REMOTE I/O
CPU only $255.00 and includes: PLCs must communicate, so why buy one that can’t? Or why pay extra so it can? With Productivity2000 you get 5 communication ports built in on every CPU. •
RS-232, RS-485, Ethernet, Remote I/O ,USB (programming) - Built in!
•
Modbus RTU, Modbus TCP/IP, EtherNet/IP, ASCII, & custom protocols - Included!
And that’s not all...remote visibility, database connectivity and mobile device access ensure that the Productivity2000 will meet all of your communication needs!
•
(1) USB port: Program, monitor or upgrade your firmware through this plug-and-play micro USB port.
•
(1) RS-232 serial port: Point-to-point connection for Modbus RTU/ASCII serial devices such as other controllers.
•
(1) RS-485 serial port: Support for up to 50 multi-drop Modbus RTU/ASCII serial devices such as operator interfaces (more if repeater is added to network).
•
(2) Ethernet ports: One 10/100 Mbps multipurpose Ethernet port capable of over 500 Modbus TCP/IP and 128 EtherNet/IP client/server connections; one dedicated 10/100 Mbps Remote I/O Ethernet port for up to 16 GS Series variable frequency drive connections and up to eight remote base groups.
Get more than you paid for…www.Productivity2000.com
Orders over $49 get FAST FREE SHIPPING Our shipping policies make it easier than ever to order direct from the U.S.!
Fast free standard shipping* is available for most orders over $49 U.S., and that includes the brokerage fees (when using an AutomationDirect nominated broker). Using our choice of carrier, we can reach most Canadian destinations within 2 to 3 days. Order by 6pm ET and in-stock orders ship the same day! *2-day free shipping does not apply to drop-ships, or orders requiring LTL transport, but those shipments can take advantage of our negotiated super-low flat rates (based on weight) that include brokerage fees. See Web site for details and restrictions at: www.automationdirect.com/canada
To see all products and prices, visit www.automationdirect.com All prices shown are U.S. Dollars
Order Today, Ships Today! * See our Web site for details and restrictions. © Copyright 2015 AutomationDirect, Cumming, GA USA. All rights reserved.
1-800-633-0405
the #1 value in automation
November/December 2016 Vol. 31, No. 7
DEPARTMENTS 4 From the editor 5 Automation upfront
The latest industry news, deal makers, and movers and shakers
19
16 Centre stage
Andrew Dolphin, Trulite Glass & Aluminum Solutions production planning manager
COLUMNS 10 Lean insights
Problem solving tools to resolve customer issues
CONTENTS
12 Industry watch
COVER STORY
Are you missing the “biggest single, lost continuous improvement opportunity?”
19 The slow climb
14 Machine Safety
Ensuring safe operations with collaborative robots
24
30 Backstory
Updating aging infrastructure is good for business
By Sreenivasa Chakravarti
Selecting components that make the grade By Brian Shuman
26 Hardwiring alternative
14
MANUFACTURING AUTOMATION · November/December 2016 MA_Murr_Nov.indd 1
23 Taking full advantage Manufacturers who embrace IoT lead the digital transformation 24 Industrial communications networks
NEW PRODUCTS 27 Machine safety 27 Automation software 28 Motors & drives 28 Robotics 29 Material handling 29 Process control 29 Communications & networking
The 2016 Canadian Manufacturing Study finds the industry is growing, slowly but surely By Alyssa Dalton
UL 508 status makes connectors a viable option for wiring electrical control cabinets By Cory Jenkins
AutomationMag.com
3
2016-10-27 9:20 AM
FROM THE EDITOR BY ALYSSA DALTON
NOTABLE TWEETS
Your resource for Canada’s industrial automation news
Using innovation to foster Canadian manufacturing
@JenniferKR A hot piece by @DavidMemex: The #IIoT or Industry 4.0: Who will win? bit.ly/2ehN87z #mfg #manufacturing
LEAN MANUFACTURING: Defining culture as an environment favourable to continuous improvement. p.10
LIGHTING RETROFITS: Industy bakery welcomes retrofit for non-energy operational savings. p.22
AutomationMag.com
Your resource for Canada’s industrial automation news
THE MAJIK
TOUCH
Ontario startup allows factory managers to act before they know there’s a problem p.18
Think Allied for Industrial Automation. More Brands. More Products. More Solutions. See it all at thinkallied.com/industrialautomation
AlliedCover_MA_Jan.indd 1
2015-12-23 1:58 PM
@johncorpcomms @AutomationMag Good read: “There has never been a time riper... to invest in smart technology” says @1seanriley bit.ly/2dLZ4Af @KPMG_Canada “When you have a good idea... take a deep breath & jump in.” - Beth Wilson, GTA Managing Partner @KPMG_Canada #WeDay
I
nnovation is an interesting concept in manufacturing. It has long been cited as an important factor of a country’s economic success, but how do you define and quantify innovation? Is there a right and wrong way to innovate? The Canadian Conference of Board recently published an op-ed in the Globe and Mail with the headline, Innovation is key to success of Canada’s manufacturing sector. “Manufacturing is still an important part of Canada’s economy,” writes Glen Hodgson, senior fellow, and Michael Burt, director, the Canadian Industrial Outlook. “However, its role in the economy has been steadily shrinking. Manufacturing employs half a million fewer Canadians today than it did in 2000. The experience of the manufacturing sector in Canada is not unique — it is declining as a proportion of the overall economy in every major developed country. Even China is seeing manufacturing’s share of its economy shrink.” Hodgson and Burt suggest several ways for Canadian manufacturers to increase their global competitiveness: seek to fit into the value chains of larger global firms; focus on specializing in high-value manufacturing segments and activities; and integrate client services into the sale of manufactured goods. “Ultimately, innovation is the key to success for manufacturing firms. It could take the form of product innovation, such as adding client services or adapting products to new CONNECT @AutomationMag
markets. Or it may come through process innovation, which could be anything from production techniques to management processes. Creating an innovation culture within Canadian manufacturing firms, sectors and clusters is likely a critical and required form of process innovation,” they say. “Ultimately, innovation will drive the productivity improvements that are required if Canadian manufacturers are to remain competitive and thrive.” This insight couldn’t come at a more perfect time. This issue’s cover story looks at the results of our 2016 Canadian Manufacturing Study, an annual survey we run in conjunction with the Excellence in Manufacturing Consortium (EMC) to help benchmark manufacturers and their yearly performance, and based on our results, very little of our economy has changed over the past year. In fact, much of the data are eerily similar to the 2015 responses, suggesting that the majority of this year’s respondents are recovering from the 2008–2009 recession with mere baby steps. (Read more about the strategies, methods and technologies used by the sector on page 19.) But we need to take bigger strides. As I wrote at the beginning of this year, with challenges come opportunities, and with opportunities come risk and reward. When putting together your New Year’s resolutions, don’t forget to include those methods. | MA
adalton@annexweb.com
AutomationMag.com
EDITORIAL ADVISORY BOARD AL DIGGINS, President and General Manager, Excellence in Manufacturing Consortium, and Chairman and CEO, Canadian Manufacturing Network DAVID GREEN, Technology and Business-to-Business Consultant KARIN LINDNER, founder and owner of Karico Performance Solutions DON MCCRUDDEN, Vice-President, Business Development, Festo DAVID MCPHAIL, President and CEO, Memex Automation NIGEL SOUTHWAY, Business Productivity Consultant and Author on Lean Thinking BILL VALEDIS, Vice-President, Precision Training, Products and Services Inc. 4
Alyssa Dalton adalton@annexweb.com PUBLISHER
Klaus B. Pirker kpirker@annexweb.com
@MFGTalkRadio Millennials will be the future of the manufacturing industry. Manufacturers have to understand what they want from an employer. ETHERNET GAINS: Acadian Seaplants capacity grows by 40 per cent with new processing facility. p.20
EDITOR
@AutomationMag
VICE PRESIDENT & EXECUTIVE PUBLISHER
Tim Dimopoulos tdimopoulos@annexbizmedia.com ART DIRECTOR
Graham Jeffrey gjeffrey@annexweb.com ACCOUNT CO-ORDINATOR
Kathryn Nyenhuis knyenhuis@annexweb.com CIRCULATION MANAGER
Urszula Grzyb ugrzyb@annexbizmedia.com DIRECTOR OF SOUL/COO
Sue Fredericks CONTRIBUTING WRITERS
Rita Aiello, Sreenivasa Chakravarti, Paul Hogendoorn, Cory Jenkins, Brian Shuman, Mike Wingrove, WSPS
Manufacturing Automation is published seven times a year by: Annex Business Media 222 Edward Street, Aurora, Ontario L4G 1W6 Tel 905-727-0077 Fax 905-727-0017 Printed in Canada ISSN 1480-2996 Publication Mail Agreement #40065710
CIRCULATION email: lmalicdem@annexbizmedia.com Tel: 416-510-5187 Fax: 416-510-5170 Mail: 80 Valleybrook Drive, Toronto, ON M3B 2S9 SUBSCRIPTION RATES Canada — $40.95 per year United States — $71.95 (US) per year and Foreign — $82 (US) per year Students — $20 per year Occasionally, Manufacturing Automation will mail information on behalf of industry related groups whose products and services we believe may be of interest to you. If you prefer not to receive this information, please contact our circulation department in any of the four ways listed above. The contents of Manufacturing Automation are copyright © 2016 by Annex Publishing & Printing Inc. and may not be reproduced in whole or part without written consent. Annex Publishing & Printing Inc. disclaims any warranty as to the accuracy, completeness or currency of the contents of this publication and disclaims all liability in respect of the results of any action taken or not taken in reliance upon information in this publication. We acknowledge the [financial] support of the Government of Canada.
AUTOMATION UPFRONT
RENEWABLES
PHOTO: L’ORÉAL
L’Oréal building solar projects at Arkansas, Kentucky plants L’Oréal USA says it will exceed its carbon emission reduction goals and build two large-scale solar projects at its manufacturing facilities in North Little Rock, Ark., and Florence, Ky., as part of its global sustainability strategy, Sharing Beauty with All. With the projects, the company said it will reduce carbon dioxide emissions by 80 per cent from 101,634 metric tons in 2005 to a projected 20,059 this year. “Reducing our CO2 emissions by 80 per cent and achieving 100 per cent renewable electricity for our U.S. manufacturing is a major milestone for L’Oréal USA,” said Fréderic Rozé, CEO of L’Oréal Americas. “The achievement is a testament to our passionate, creative and innovative teams who have pushed us to go beyond our original ambitions.” The North Little Rock plant, in partnership with Scenic Hill Solar, will house a 1.2 MW array that will be the third largest commercial solar array and the fourth largest solar project in Arkansas. The 4,000 solar panel installation in North Little Rock is scheduled to be operational by mid-2017 and will reduce carbon emissions in Arkansas by 1,326 metric tons per year, equivalent to eliminating nearly 3.2 million miles traveled by passenger cars per year, according to EPA Greenhouse Gas Equivalencies. L’Oréal first installed a solar array at its North Little Rock plant in 2012, which now supplies the equivalent of 100 percent of its outdoor lighting needs (18,000 kWh/year). The 446,691-squarefoot factory has operated in the state for over four decades, and is home to cosmetics production for brands including Maybelline, L’Oréal Paris, Essie and Lancôme. The Florence plant, also in partnership with Scenic Hill Solar, will house the largest commercial solar array in Kentucky at 1.5 MW. Construction of the
project will start late 2016 and will consist of approximately 5,000 solar panels. The array is projected to cut CO2 emissions in Kentucky by approximately 1,195 metric tons per year, equivalent to eliminating over 2.8 million miles traveled by passenger cars per year, according to EPA Greenhouse Gas Equivalencies. The 687,000-square-foot plant, where haircare products are
MANUFACTURING AUTOMATION · November/December 2016 MA_Beckhoff_Nov.indd 1
“Major milestone”: L’Oréal USA says its new large-scale solar projects will reduce carbon dioxide emissions by 80 per cent.
made for the Garnier, L’Oréal Paris, Matrix, and Redken brands, is the company’s largest
manufacturing site in the U.S. and its largest worldwide by tonnage of products produced.
AutomationMag.com
5
2016-10-21 9:24 AM
AUTOMATION UPFRONT
Lafarge completes $20M modernization upgrade at Alberta plant Lafarge Canada says it has completed “major” modernization and environmental upgrades at its Exshaw, Alta., cement plant, resulting in an increase of production capacity from 1.3 million metric tonnes per year (tpy) to 2.2 million metric tpy. According to the company, the technology upgrades led to a 60 per cent reduction in sulphur dioxide emissions, a 40 per cent reduction in nitrogen oxide emissions, and a “significant” reduction in fugitive dust and noise coming from the plant’s equipment. The plant has also achieved zero water discharge from its operations, said the company in a statement. Physical construction began
in 2013, with more than 600 contracted employees on site at construction peak in addition to 160 permanent employees. Modernization upgrades focused on the kilns, which are “the heart” of the cement-making process. In November 2015, kiln 4 was shut down, and the company invested $20 million in kiln 5 to meet new emissions targets by retiring less efficient gravel-bed filter technology. A new kiln 6 was constructed with a “state-of-the-art” baghouse to collect particulates, said the company, as well as a vertical raw mill, the EcoDome storage facility, a pre-heater tower and a vertical cement mill to complete the expansion. Lafarge said the team “achieved a very strong safety record, hitting nearly three million hours without a lost time incident.” “It is an incredible achievement, completing a project of this scale. Completing it safely takes focus
Academic partnership: The collaboration aims to accelerate the implementation of Industry 4.0 advanced manufacturing concepts.
and energy and I applaud the team for its dedication to this goal,” says René Thibault, president and CEO, Lafarge, Western Canada. “By all accounts we consider the project to be a success, cementing our long term commitment to Exshaw, Alberta and western Canada.” EDUCATION
Kwantlen Polytechnic partners with Siemens for Mechatronics Certification Program
The PROGRAMMABLE Size 25 shaft encoder that goes anywhere Program your CPR, output, and waveform on-site! CPR – any resolution from 1 to 65,536 Waveform – choose from 32 options Output type – 6 different outputs Designed for an industrial environment, the Model 25SP comes standard with dual bearings rated 80lbs axial or radial, and offers sealing up to IP67. Call EPC today to learn how the Model 25SP can be your encoder solution. 1-800-366-5412 • www.encoder.com
6
British Columbia’s Kwantlen Polytechnic University (KPU) and Siemens Canada have announced a new collaboration aimed at accelerating implementation of Industry 4.0 advanced manufacturing concepts and addressing the technical skills gap in Canada. Expected to begin early-to-mid 2017, the university will offer the Siemens Mechatronics Systems certification program in association with the Siemens Canada Engineering and Technology Academy (SCETA), which was established in 2014 and based out of Siemens Canada’s head office in Oakville, Ont. According to the parties, the “highly specialized” program is the first of its kind to be offered in B.C. The university will also establish a mechatronics lab facility in Surrey, B.C. Located at its trades and technology campus in Cloverdale, the facility will serve as the training centre for students
November/December 2016 · MANUFACTURING AUTOMATION
@AutomationMag
MA_Encoder_Nov.indd 1
pursuing the Siemens Mechatronics Systems certification program. “The manufacturing sector in Canada and globally is undergoing rapid and dramatic changes as industry enters the fourth industrial revolution — referred to as Industry 4.0 — which involves the mass adoption of digitization and advanced technologies. Manufacturing systems are becoming increasingly complex and digitalized and these systems require qualified highly-skilled individuals with the knowledge required to design, operate and maintain them,” said Siemens Canada in a statement. “This agreement is a significant step forward for KPU as it implements its unique polytechnic university mandate. By partnering with Siemens, a world leader in engineering and manufacturing technology education, KPU reaffirms its commitment to a future-focused, high-quality and globally relevant advanced manufacturing training program,” said Dr. Salvador Ferreras, provost and vice president academic, KPU. Equipment in the lab will include electrical and mechanical components purchased by KPU from approved suppliers, including Festo Didactic and programmable logic controllers (PLCs) from Siemens Canada. The addition of the lab will also set the foundation for future academic offerings at KPU, including a diploma in advanced manufacturing. “Innovation, productivity and
2016-10-17 9:25 AM
PHOTO: KWANTLEN POLYTECHNIC UNIVERSITY
INVESTMENT
Your Global Automation Partner
CH A R T W E L L
Your productivity is priority number one at Turck. Keeping your automated operation running at peak performance with maximum up time is our mission. We do it by providing an extensive line of durable, dependable products and unsurpassed customer service and support. Turck Works!
uproxÂŽ3 Inductive Proximity Sensors
QR24 Rotary Inductive Sensors
IO-Link Solutions
Third-generation factor 1 sensors offer compact
Expanded line of contactless rotary position
Our solutions are designed for reduced
design and the farthest sensing range of any
sensors provides superior performance and a
machine costs, improved machine availability
inductive sensors on the market.
wide range of outputs options.
and enhanced process efficiency.
A global leader in industrial automation technology, Turck Chartwell provides best-in-class products, solutions and support.
Call 1-877-513-7769 or visit chartwell.ca
AUTOMATION UPFRONT
NBCC Saint John Campus receives infrastructure funding The New Brunswick and federal
governments are investing a total of $15.89 million at New Brunswick Community College (NBCC) Saint John campus for a new trade education facility. The funding is being provided though the Post-Secondary Institutions Strategic Investment Fund. According to NBCC representatives, the new facility will “improve the scale and quality of the trades programs at the Saint John campus.” The investment will also help to build multi-functional spaces for future classroom and shop programming needs. The existing welding shop will be demolished. “NBCC makes a significant contribution to New Brunswick’s socio-economic prosperity,” said Susan Murchison, chair of the NBCC board of governors. “Aging infrastructure is a challenge to maintaining and growing that contribution. This investment in a new trades facility at our Saint
SOLUTIONS
Production boost: Vicwest says the new centre was “designed for maximum efficiency and output in a smaller facility footprint.”
John campus will ensure that NBCC can continue to play an important role in developing a highly-skilled workforce here in New Brunswick.” The provincial government will invest $8.67 million, while the federal government will provide $7.22 million. “By working with the Trudeau government, we are getting things done to advance New Brunswickers priorities of economic growth, education and health care,” said premier Brian Gallant. “This project will allow NBCC in Saint John to strengthen its trade courses. We must value trades as they are crucial for our economy.” OPERATIONS
Vicwest opens Centre of Excellence manufacturing facility in Alberta
FOR ALL YOUR
INDUSTRIAL, AUTOMATION AND CONTROL NEEDS Automation, Safety, Motor Control, Drives, Programmable Controllers, Operator Interfaces, Sensors, Networking Solutions, Enclosures, Test & Measurement. To locate your nearest WESCO Branch or shop online visit buy.wesco.ca 1-866-WESCOCA (937-2622) | wesco.ca
Vicwest celebrated the recent grand opening of its new manufacturing facility in Acheson, Alta., with a ribbon-cutting ceremony and a $5,000 donation to the Alberta Food Banks. In addition to the grand opening, Vicwest is celebrating 85 years as a Canadian manufacturer of steel roofing and cladding for the residential, commercial and agriculture industries. The centre was “designed for maximum efficiency and output in a smaller facility footprint,” said the company in a statement, adding that it features: • Optimized floor space achieved
8
At 60,000 square feet, the facility has 18 full-time operators on the floor. Forty-five new jobs were created as a result of the new facility. “Our new Centre of Excellence was built based on advanced quality manufacturing systems, and we are proud to introduce an innovative and more sustainable facility that truly keeps future generations in mind,” said Paul Lobb, president and general manager, Vicwest Building Products. INTERNATIONAL AUSTRALIA
Ford ends car manufacturing in Australia after 91 years The last Australian-made six-cylinder Ford Falcon XR6 rolled off the Broadmeadows plant in Melbourne, Australia, last month, marking the end of the car maker’s 91-year manufacturing history in the country.
November/December 2016 · MANUFACTURING AUTOMATION
@AutomationMag
MA_Wesco_Nov.indd 1
through coil cars that load uncoiling machines and reduce the length of mills; • Increased mill operations speed as a result of VF drives and servo controls; • Lean principles applied to material flow from loading to shipping, enhancing overall efficiencies by reducing time and costs; • Automated stackers at the end of mills; and • Future automated wrapping of materials.
2016-10-19 11:11 AM
PHOTO: VICWEST
success for Canadian manufacturers are directly tied to the skills and abilities of their employees,” said Robert Hardt, president and CEO, Siemens Canada. “We are honoured to collaborate with KPU to bring mechatronics training to British Columbia, offering students the opportunity to pursue this globally recognized certification that will ultimately help prepare them to succeed in Canada’s top industries upon graduation.” The Mechatronics certification courses, designed to be integrated into the school’s existing curriculum, will be offered to students in two levels and taught by KPU faculty trained at the Siemens Technik Academy in Berlin, Germany.
The closure of the facility will result in approximately 600 lost jobs, said the company. According to The Associated Press, Ford will continue to “sell and service imported cars in Australia and Australia-based engineers will help develop designs of vehicles that will be manufactured overseas.” In 2013, Ford — along with General Motors and Toyota — announced it would cease production of vehicles in Australia, as a result of “high production costs, distance from potential export markets and increasing competition,” reported AP. DEAL MAKERS
Advanced Motion & Controls welcomes Ross Controls as strategic partner
PHOTOS: MAGNA INTERNATIONAL
Barrie, Ont.-based Advanced Motion & Controls (AMC) has announced the addition of Ross Controls to its line up of global partners. “The Ross brand is globally recognized as the leader of pneumatic safety products and solutions, we are very pleased to be able to partner with such a powerful player in this marketplace,” said Mark Schick, president. “Leveraging our current product lines the Ross brand will enhance our offering and expand our presence in Canada’s leading industries.” “With a full complement of sales, engineering and
manufacturing support, we have been able to provide our customer base with the expertise required in today’s competitive marketplace. The addition of the Ross brand will only reinforce our commitment to providing our customer base with the best solutions for their challenging applications,” according to a company statement.
Magna to acquire BOCO Group of Companies Magna International says it will increase its product portfolio and engineering capabilities through its acquisition of the BOCO Group of Companies, an automotive supplier of latches, hinges and strikers. As a result of the acquisition, BOCO’s two facilities located in Wuppertal, Germany, and Tianjin, China, and its approximately 450 employees will be integrated into Magna Closures, an operating unit of Magna. “We believe BOCO is an excellent fit in terms of technology, footprint and customers, and we look forward to working together to further grow our business,” said John O’Hara, president of Magna Closures. “BOCO’s product and processing know-how and engineering strength also provides additional global growth opportunities for us going forward, particularly with automakers based in Germany.” The transaction is expected to close in the fourth quarter of 2016,
.
Making moves: BOCO’s German and Chinese facilities and employees will be integrated into Magna Closures, an operating unit of Magna. MANUFACTURING AUTOMATION · November/December 2016
AutomationMag.com Hiwin_MA_Jan.indd 1
9
2015-12-10 12:54 PM
AUTOMATION UPFRONT
Growth strategy: Rockwell Automation says it has acquired Maverick Technologies to help deliver control and information solutions.
subject to regulatory approval. Magna is a global automotive supplier with 309 manufacturing operations and 99 product development, engineering and sales centres in 29 countries. Meanwhile, BOCO has annual sales of more than 100 million Euro and its customers include the BMW Group, Daimler and Audi.
incorporation of this know-how, we complement our product portfolio and furthermore gain a valuable development resource,” said Frank Stührenberg, Phoenix Contact CEO.
Phoenix Contact acquiring Perle Systems
Rockwell Automation says it has acquired Maverick Technologies in a move to “expand domain knowledge and help deliver innovative control and information solutions” to customers. According to a statement from Rockwell Automation, the acquisition will help support its growth strategy to “help customers increase global competitiveness by adopting The Connected Enterprise, a vision that connects information across the plant floor with the entire enterprise to drive new business value. This is particularly important to process customers whose uptime and continuous performance are critical.” “We will continue to deliver our domain expertise, now with the power of a Fortune 500 industrial automation leader at our side,” added Paul Galeski, Maverick founder and CEO. “This creates the best combination available to help uncover the benefits of information that drives performance in process industries.”
Phoenix Contact GmbH & Co. KG says it is expanding its expertise in industrial network technology with its recent acquisition of Canadian network specialist Perle Systems Ltd. Based in Toronto, Ont., Perle Systems provides products and solutions for industrial networks. Since 1976, the company has been developing and selling media converters, industrial Ethernet switches, and serial devices. The company will continue its business operations under its own name. “It is the objective of Phoenix Contact to expand the new subsidiary to another competence center for industrial networking within the Group,” said the company in a statement. “Perle Systems has extensive product know-how and successfully operates a global online business. This constitutes an important reinforcement for us with regard to the digitalization of business models. Due to the 10
@AutomationMag
Rockwell Automation to purchase Maverick Technologies
Andreas Sobotta will lead as the CEO and general manager of Pilz Automation Safety Canada. “I am very excited to join such an innovative company which spends over 20 per cent of their global sales in R&D. The Canadian team is very enthusiastic and I look forward to growing with them,” says Sobotta, who has held various leadership roles at Davis Controls, Festo, Siemens, Phoenix Contact and, most recently, Hammond Manufacturing. The company describes him as an “experienced professional with many years in the electrical and controls world.” Jeff Austin has been announced as the new operations manager for Huffman Engineering, a CSIA certified control systems integration company. In this role, Austin will oversee a team of engineers and technicians who develop and execute turnkey automation projects for manufacturing and utility customers. “ Baldor Electric announced Ryan Waite has been named the director of motor product management for its global NEMA motor business, where he will be responsible for the “rapid global growth” of Baldor•Reliance motors sales and implementing the strategic vision for the business. He previously held a range of positions, including manufacturing engineering manager, plant manager, and most recently, director of manufacturing. Waite has been with the company since 1990. Joe Nitiss has been named CEO of Rockford Systems,
a manufacturer of machine safeguarding products solutions, effective immediately. Nitiss were previously general manager of the North American business unit of Elster, a provider of gas, electricity and water meters. Capitalizing on his experience with Fortune 500 companies, Nitiss will be “leading Rockford Systems in advancing its place as a trusted supplier and advisor for a broad range of machine applications in industrial markets,” said the company. Chris Pfeiffer will support Lauren Manufacturing’s strategic plan for growth as the company’s new executive vice president, as the company strives for a “future of expanded revenue, increased employee engagement and continued focus on operational excellence.” President Lisa Huntsman said Pfeiffer’s commitment to continuous improvement and ability to connect with people made him the right choice for this new position. Pfeiffer will remain president of Lauren AgriSystems, a role he has held since he joined the business in 2012. Unex Manufacturing says it has realigned some of its sales territories in an effort to better serve the needs of customers in those areas “with a greater level of service and more extensive product support.” There are two personnel changes that affect Canada. Jay Cox, catalogue/ Canadian sales manager, will no longer be servicing Canada, but taking over all business in Northeast U.S. He has been with the company for three years. Meanwhile Tom Wagner, Central West sales manager, will take over all business in Canada. He has been in the material handling industry for 20 years in key management positions, according to Unex. | MA
November/December 2016 · MANUFACTURING AUTOMATION
PHOTO: ROCKWELL AUTOMATION
MOVERS & SHAKERS
The Only Switch that Matters Is the One You Need And We’ve Got It
In stock and ready-to-ship. See it all at thinkallied.com/switches
1.800.433.5700 © Allied Electronics, Inc 2016. ‘Allied Electronics’ and the Allied Electronics logo are trademarks of Allied Electronics, Inc.
An Electrocomponents Company.
INDUSTRY WATCH BY PAUL HOGENDOORN
Paul Hogendoorn (paulh@getfreepoint.com) is co-founder of FreePoint Technologies, “Measure. Analyze. Share.” (Don’t forget to share!) Visit www.getfreepoint.com for more information.
Meet Jim — not your average Joe
I
met Jim last year when I visited the plant he works at, which is near Ottawa. He’s a down-to-earth guy, about my age (getting up there!), and has a knack for figuring things out and getting them done. He’s been doing it for 38 years. At first glance, he’s the kind of guy you wish you had in your plant, or perhaps, think you already have — but as you read on, you’ll see his story is much more than that. Jim is now intentional and committed to the continuous improvement process, but he wasn’t always that way. He started his first job at nine years old — delivering papers — and he has worked every year of his life since. He heeded his mother’s advice that “it’s work and work ethic you need to worry about,” and for many years that was enough. In his youth and early years, he spent all of his weekends and summers working, and was never out of a job; from washing dishes, cooking food, stocking shelves, renting cars and doing oil changes, to steadier and higher paying factory jobs, where he progressed to the point of operating the big machines. Improvement) department. He worked in About six years ago, 15 years into his job a process technician role for two years, and running the big machines, he reached the top then in 2012, moved into a management role. of his pay scale as a “lead hand” — there was That in itself would be a great continuous not much left to learn and nowhere else to go. improvement story, but the story doesn’t end After much reflection, and with encourage- here. ment and support from his wife, he decided As a manager, he took a keen interest in to pursue other positions at the company, but the development of others, especially people it soon became apparent his computer skills around his age or a bit older — those who had were inadequate. Microsoft Excel been there for two or three decades; and PowerPoint were a mystery to employee with great working skill him, and Word was equally dauntand experience, but little or no exing. Younger people with more Simply posure to new technology. Some did computer skills, but not nearly as focusing not have cell phones or computers, much manufacturing skill, had the on the or experience with email and mesclear advantage. saging systems. In my mind, this is elimination At the time, his daughter was at- of negative perhaps the biggest single, lost contending T.R. Leger School of Adult, attitudes tinuous improvement opportunity Alternative & Continuing Education in many manufacturing companies does not so he looked into the curriculum, today. The tactile experience our and to his surprise, found that it of- guarantee seasoned people have is overlooked fered courses that suited his needs. that good and not taken advantage of because On his days off, and on his own attitudes will they lack basic computer skills — volition, he enrolled. (It was, after survive, let skills that are quite easily taught. all, his own personal continuous alone thrive. Whatever risks there are to training improvement initiative.) them are quickly mitigated by the He was nervous and intimidated at first, but fact that most of these people have already he soon felt comfortable. There were about demonstrated their loyalty and dependability a dozen people in the class, including high — things that can’t be taught or calculated. school students, new immigrants, and other (Someone that has been with you for 20 years, people his age there for a reason similar — to and still has 10 or 20 in the tank, is a far safer face their fear of computers and all things IT. bet to stay with the company than someone After completing the initial course, he felt hired fresh.) confident enough in his abilities to take a posJim had an individual on his team that ition within the company’s CI (Continuous needed to be moved to an office position to 12
@AutomationMag
accommodate a health condition. The person was basically computer illiterate, but the new role was 80 per cent computer related. Remembering his own experience, Jim recommended this person be sent to a similar program he attended. The company agreed. A couple weeks later, the individual returned to work like a new man, certain he could find answers to any computer-related issues that might crop up for him. More than new computer skills, he gained a confidence that transformed his attitude from fear of failure to one where new challenges were welcomed and learning opportunities embraced. He now routinely creates complex Excel spreadsheets, edits documents in the company’s document control system, and effortlessly communicates with co-workers electronically. The change was so dramatic it wasn’t long before other managers and co-workers started to notice. Some wanted to know where to send their people, while others wanted to go for the training themselves. Other departments began to send people, and the story repeated; every person that received the training became a more valuable employee of the company. Jim made sure all employees in his department went through the program he did. Every plant I visit has a lot of people with a tremendous wealth of experience and potential, ready to be tapped into; they just need the chance to learn a few new skills. All it may take to get started is one person like Jim to make it his mission in your plant. He may be your average guy, but he’s no ordinary Joe. | MA
November/December 2016 · MANUFACTURING AUTOMATION
• Onboard communications • Graphic LCD keypad display • Advanced configuration PC tool • Multi-pump and fan control applications • Onboard Safe Torque Off • Active energy control algorithm • Real-time clock with battery backup • 5% DC link choke
Improved efficiency. Lower energy costs. Better safety and reliability. That’s what customers asked for; that’s what the new PowerXL DG1 delivers. It’s loaded with today’s most sophisticated semiconductor technology, including standard Subscribe to Eaton Insights eNewsletter to stay up to date on the latest news and products. eatoncanada.ca/subscribe
communication protocols and I/Os. All backed by Eaton’s long history of excellence. Depend on Eaton. Canada does. Learn more about the PowerXL Series Adjustable Frequency Drives. http://bit.ly/1lvQoLV
MACHINE SAFETY
Workplace Safety & Prevention Services (WSPS) is a leader in providing impactful risk management solutions, boasting unparalleled health and safety expertise, insight and solutions. Learn more at wsps.ca.
BY WSPS
Five ways to help ensure safe operations with collaborative robots
Types of collaborative operations CSA standard Z434-2014, Industrial Robots and Robot Systems, categorizes four types of collaborative operations according to the degree of collaboration between humans and robots.
• Safety-rated monitored stop Equipped with safety-rated stop functionality, the robot stops when in the collaborative workspace at the same time as an operator. Once the human has left the collaborative workspace, the robot can resume operating. This type of collaboration involves occasional interactions between human and robot, and can eliminate the need for operators to load parts into intermediate set jigs or parts nests, and manually restart the operation. “It’s more efficient,” says Vomiero. • Hand guiding This enables the operator to guide the robot with a joystick type control located near the end-effector and equipped with an enabling device and emergency stop. This replaces the traditional, and complicated, robot pendant. A manual reduced safety-rated speed function restricts robot speed to a safe limit. • Speed and separation monitoring The human and robot work 14
@AutomationMag
independently within the same space. Robot speed varies based on a safe separation distance between human and robot. If the human comes too close, the robot operation stops. Among the safety features: safety-rated speed functionality, external safety presence sensing devices (i.e., safety laser scanners or cameras), and internal safety-rated soft limits to monitor the human’s position with respect to the robot. The robot acts as an “assistant” to the operator. • Power and force limiting “Most people think of this type when we talk about collaborative robots,” says Vomiero. “It’s the only operation where you can have physical contact while the robot is in motion.” Either inherent robot design parameters or on-board safety-rated sensors and control systems limit the power output and force exerted. To further minimize risk, the physical structure is often padded and corners are rounded. Five ways to reduce risk “With the exception of power and force limiting robots, you still require a certain degree of separation, as well as safeguarding devices,” says Vomiero, adding that you must also ensure the robot’s safety functions are properly designed, implemented and used. “For instance, setting up our safe zones and distances appropriately.” Here are
With built-in safety limits, sensors and other safety functionality, “cobots” offer exciting benefits.
COBOT An increasingly popular term for collaborative robots
some key safety activities. • Familiarize yourself with CSA standard Z434-2014, Industrial Robots and Robot Systems. “It’s the first step in protecting workers,” says Vomiero. • Ensure you have a strong risk assessment process to determine what safeguarding devices are needed, as well as safe zones, speed, force and power limits for every possible collaborative scenario. “Risk assessments are the cornerstone of the CSA robotics standard, and are mandatory.” Because of the specialized nature of robotics, consider bringing in an outside expert to help develop a robot-specific risk assessment. • Create a checklist before you purchase to ensure the robots have the right safety features, meet the necessary requirements, and are compliant with the CSA standard and regulations. • Develop and train workers on safe operating procedures based on both the integrator’s information for use and manufacturers’ instructions. Train everyone who may come into contact with the robot, from operators to maintenance. • Be sure to include robots and robot cells in monthly inspections. “It’s important to ensure robotic equipment continues operating in a safe manner, and to stay on top of hazards that may develop after installation and over the life of the system,” cautions Vomiero. | MA
November/December 2016 · MANUFACTURING AUTOMATION
PHOTO: UNIVERSAL ROBOTS
C
ollaborative robots are poised to take off in the next few years, says WSPS consultant Robert Vomiero. With builtin safety limits, sensors and other safety functionality, “cobots” offer exciting benefits — they’re able to work more closely with humans, can be cheaper and easier to integrate and maintain, and promise better cycle time and productivity. But this doesn’t mean organizations anxious to embrace the new technology can rest easy when it comes to health and safety. Crushing and impact hazards remain, requiring special safety measures and a greater emphasis on certain aspects of your health and safety program.
New Ti480
TiX580
Stunning 640 x 480 resolution
Surprising affordability • Experience 4-times the resolution power in an “everyday” rugged camera • Detect small temperature differences critical to troubleshooting— leading to more accurate problem identification
Fluke infrared tools are truly “built for purpose”. Learn more at www.fluke.com/640x480
Infrared images are for illustration purposes and may not have been taken by the models shown.
©2016 Fluke Corporation. 10/2016 6008587a-en
LEAN INSIGHTS
Rita Aiello, P.Eng, is a professional industrial engineer working for Ply Gem Canada as director of continuous improvement, leading the quality department and manufacturing engineering teams.
BY RITA AIELLO
What’s the problem?
O
Figure 1
as targets for our problem solving. This year, engineering, quality and production teams have proposed changes to our problem solving model for enhanced corrective action, specifically with more focus on managing the corrective action plan with engineering/management conducting the facilitation, project management and tracking. It involves two main tools, both using our problem solving model:
Figure 2 16
@AutomationMag
1. In-line/production continuous improvement (CI) form This consists of one main page, handwritten by shop floor employees and first line leaders. This is a hybrid model of the standard Cause and Effect diagram and the 5 Why methodology. See Figure 1. 2. Full corrective action form
Managed by engineering, this is one main page that involves all parties using the process in Figure 2. Both use our standard problem solving process (refer to Figure 3). The majority of successful solutions have come from the employees who work in the assembly area. The cause and effect diagram (Figure 1) must be completed with the following staff present:
Figure 3 November/December 2016 · MANUFACTURING AUTOMATION
FIGURES: PLY GEM CANADA
ver the past few years at Ply Gem Canada, we have had iterations of problem solving models used on our production shop floor. All were centred on capturing employee engagement and real information. We have found that the more refined the front-end information has been, the more we are able to define and quantify issues which impact our customers. The common goal has been to use systematic problem solving to permanently resolve customer issues within manufacturing. The challenging upfront work was to accurately define the problem based on factual information. We have used our non-conformance form (NCF) process to highlight customer defects which input into our problem solving methods. Over the past two years, our NCF data has expanded beyond internal defect reporting to include more externally reported information from service and sales departments. This vehicle allows problems to be quantified and includes trips to site for production, engineering and production groups. This collaborative effort to collect meaningful data from our service teams positions customer issues
1) A minimum of 15 per cent of the employees who work in the assembly area (the more, the better!) or all the staff performing a certain task depending on the problem found; 2) Supervisor of the area; 3) Production manager of the area; 4) Engineering support staff; and 5) Quality department staff. *optional as required: purchasing or maintenance staff The expectation is that each production line comes together to tackle at least one production CI per week. These sessions are prescheduled in a shared calendar to ensure all support staff knows when they are and the production manager can change the time as needed. The CI topics are chosen mainly from customer service reported data, however a production manager can choose whatever opportunity for improvement they see fit. All data is located on a shared drive on our Intranet (even the scanned copy of the handwritten cause and effect diagram) for transparency. This way our service department can also reference the actions being taken. In the beginning, it was very difficult for production supervisors and managers to commit their line staff to participate in this regularly scheduled session, and to be honest, it still is. Without line staff present (the people doing the real work), there is no real CI session. Top-down approaches where supervisors and managers implement solutions for the assembly staff without them typically result in superficial solutions that are never sustainable. We need our staff to be motivated about making improvements; this can only happen if they are part of the solution plan. More recent success of our production CI program has been reliant on empowering the staff who do the assembly work. It is through them where more effective procedures can be
discovered and captured into our work instruction standards. This is where our leadership is key; allowing time for regular CI events and ensuring knowledgeable staff are present to contribute. Results of our production CI system are not only measured by the specific gains within our process stabilization, but it also leads to a culture shift over time. If assembly staff and line
supervisors can become better decision makers and problem solvers, management will have more time to focus strategically. Over the past five years, this in-line CI model has been evolving due to feedback from the year prior. All the people in my engineering, quality teams and production teams who are working on making this process a success have a strong will for
improvement. Without that, it doesn’t matter which CI program you put in place, it won’t be able to survive. Today we have more staff dedicated to the program than ever, and we understand that status quo is not good enough. Through our in-line CI program, we are connecting our customers and employees and turning customer issues into permanent solutions. | MA
Permanent Precision, Excellent Backlash Stability • Harmonic Drive® or Harmonic Planetary® gearheads • Zero backlash and low backlash versions • Ratios: 3:1 - 160:1 • Peak Torque: 3.9 N•m - 3940 N•m • Sizes: 40mm - 230mm • Output Configurations: Hollow Shaft, Flange, Keyed Shaft, Smooth Shaft
TM
Harmonic Drive LLC 247 Lynnfield Street Peabody, MA 01960 800-921-3332 www.HarmonicDrive.net
Electromate Industrial 6221 Highway 7, Unit #15 Vaughan, Ontario, Canada L4H 0K8 (877) SERVO98 (737-8698) www.electromate.com
Harmonic Drive®, Harmonic Planetary® and Quick Connect® are registered trademarks of Harmonic Drive LLC. Electromate Industrial Sales is the exclusive Canadian distributor of Harmonic Drive® products (except the Province of Alberta).
MA Quick Connect.indd 1
MANUFACTURING AUTOMATION · November/December 2016
MA_HarmonicDrive_Oct.indd 1
9/20/16 11:59 AM
AutomationMag.com 17 2016-09-22 1:21 PM
CENTRE STAGE
Manufacturing AUTOMATION chats with Andrew Dolphin, production planning manager at Trulite Glass & Aluminum Solutions, to learn how recent automation investments are improving the manufacturer’s Woodbridge, Ont., fabrication and distribution operations.
18
@AutomationMag
I graduated, they offered me a job in production planning and I thought I’d give it a try and have just stuck around. MA: What do you enjoy most about your job? AD: My favourite part of my job is that every day is different. Our business is very custom so each order has unique challenges we have to work through. I also enjoy the team environment we have at Trulite — we have many knowledgeable and talented people here. It makes coming in for work a lot of fun. MA: What advice or words of wisdom would you give to a young person considering a career in manufacturing? AD: For anyone who wants to go high up in management in manufacturing, I would really recommend they get a huge knowledge of machinery and financials because the majority of the biggest decisions that a company makes typically involves those two areas. | MA
in a huge increase in our silk screen business. Architects have turned that requirement, which was meant to be a standard dot pattern, into an opportunity to present custom design features for their building, so everything we’re doing now has to have unique patterns. This makes standardizing the plant a lot more difficult than before. MA: Describe your job to us — how did you get started at the company and what do you do now? AD: I oversee quoting, materials, production planning and the shipping department, so my
day-to-day responsibilities are really different depending on what’s going on that day. Every morning we review late and upcoming due orders to make sure we are on track for on-time delivery, and we also have supervisor/management production meetings where we go over the production numbers from the day before and safety [best practices]. I’ve been at Trulite for 14 years in total. I started in the summers, working in the shop tempering glass, while I was studying economics at the University of Guelph. I worked here every summer and when
Open casting call! We need your help to identify manufacturing newsmakers in the Canadian industrial automation industry! These individuals bring fresh thinking to the workplace, display leadership principles, and inspire others in the business. Does someone you know fit the bill? Get in touch with our editor Alyssa Dalton at adalton@ annexweb.com and tell her who you think should be spotlighted on the Centre Stage in an upcoming issue of Manufacturing AUTOMATION.
November/December 2016 · MANUFACTURING AUTOMATION
PHOTO: A. DOLPHIN
MA: Tell us about the recent plant upgrades at Trulite Glass & Aluminum. AD: We are an architectural glass fabricator, and two of the biggest trends we see now in our industry are the automation of tasks and the customization of projects. This creates a bit of a problem because the two don’t really mesh well. In terms of plant upgrades, over the last year and a half, we have installed a second automatic cutting table, a second horizontal CNC for drilling and notching, and added seven new cranes with vision systems for people around the plant. The new cutting table was implemented about nine months ago, the CNC about eight months ago, and the cranes were installed about 15, 16 months ago. Now we have two tables so we’re able to specify what glass goes where. This has really opened up our production and cutting operations, and we’ve seen increases to our square foot per man-hour. Our drilling operations has been significantly boosted too, since before we only had one really big CNC and it required a lot of setup time and this one has really cut that setup time down. Meanwhile, the crane and lifting assist has allowed us to utilize our labour force in a much better way, by giving them various tasks to do instead of just having them lift glass all day. With regards to glass customization, there have been a lot of changes to code lately, and the most significant one is probably the addition of bird-friendly requirements to the first four floors or 40 feet of a building. This requires patterns on the glass so that the birds can see, and this has resulted
COVER STORY
THE SLOW CLIMB The 2016 Canadian Manufacturing Study finds the industry is strengthening, slowly but surely BY ALYSSA DALTON
T
his year marks the 11th annual Canadian Manufacturing Study, and based on our results, very little of our economy has changed over the past 12 months — while a handful of percentages did increase, many of this year’s numbers closely mirror our 2015 data. Conducted by Manufacturing AUTOMATION in conjunction with the Excellence in Manufacturing Consortium (EMC), the annual survey is designed to give insight into the Canadian manufacturing sector, offering company snapshots and year-to-year comparisons of Canada’s industrial performance. For the seventh consecutive year, total annual production has increased for more than half of respondents (56.26 per cent), a minuscule difference from last year’s 56.34 per cent. Around 74 per cent of respondents say they plan to expand their production within Canada over the next three years, a slight bump up from last year’s 72 per cent. Other top locations for expansion include the United States, Asia and Europe. Respondents also say they plan to grow their sales and service, engineering/R&D, and marketing. One of the biggest differences we saw in
our data related to the average hourly wage for plant workers — according to this year’s responses, the 2016 hourly wage is $24.89, a jump up from last year’s $22.41 average. It’s interesting to note nearly 35 per cent of respondents expect to see improvements sometime in 2017, while 18 per cent perdict a turnaround by 2018 and beyond. By the time our next survey rolls out, I imagine we’ll see if those who go slow and steady really win the race.
HIGHLIGHTS: • Sixty per cent of respondents say they do not use robotics in their manufacturing operations; meanwhile, just under eight per cent say robotics are integral to their operation. Both figures are in line with last year’s data. • Like last year, Canada was once again listed as the number-one location for expansion, as well as the top spot respondents are most interested in acquiring new customers from. The United States, Asia and Europe were named other top locations for expansion. • Nearly 40 per cent of respondents anticipate their company will expand in the next 12 to 18 months, mirroring last year’s
39.86 per cent. • Around 55 per cent of respondents say they have seen an increase in demand from current customers, slightly up from last year’s 51.76 per cent. • Production was the top area cited for expansion over the next three years by 59 per cent of respondents, similar to the 60 per cent from last year, and the 61 per cent from 2014. • It’s promising to see the average hourly wage is up approximately $2.50 over last year’s $22.41 average. • About 72 per cent reported annual revenues below $100 million, this is a touch lower than last year’s 75 per cent. Numbers on the higher end of the scale saw an increase however, in particular the percentage of respondents who saw annual revenues of more than $1 million grew to 6.47 per cent from last year’s 4.11 per cent. • More than 40 per cent of respondents — 43 per cent to be exact — say they expect to purchase new software in the following 12 months. Other top responses include production control (31.65 per cent), material handling (30.38 per cent) and CNC machining/milling (27.85 per cent). • The availability of skilled labour, labour costs, and increased competition from foreign countries were selected by respondents as the top barriers to their company’s future competitiveness. Energy costs and the cost of equipment/automation upgrades followed closely behind as common challenges for manufacturers across the board. | MA
WHAT OUR RESPONDENTS SHARED WITH US “We have emerged from being dumped by our parent, and on our own merit recouped orders, regained customers and are pressing ahead with leading edge products.”
MANUFACTURING AUTOMATION · November/December 2016
“The packaging industry is booming right now.”
“Our business has remained stable, most of our customers are in the U.S. and most of our sales are in USD but most of our expenses are in CAD funds.”
AutomationMag.com 19
COMPANY SNAPSHOT What is your current title?
Owner/partner
Senior executive (CEO, president, CFO, COO, VP, etc.)
19.05%
Manager/supervisor
Senior manager/ director
16.40%
8.47%
Professional
23.28%
12.17%
What industry sectors do your products serve?
What type of manufacturing does your company engage in?
(Note: respondents were able to select more than one industry as their primary industry.)
40.21%
27.51%
32.28%
Process
Discrete
Both
What other sectors do you serve?
6.36%
Less than 5 years
5 to 9 years
13.87%
74.57%
more than 20 years
10 to 20 years
11.64% 5.29%
How many people work at your company? Fewer than 25
37.57%
25 – 49 people
13.23% 12.17%
64.18%
35.82%
50 – 99 people
Aerospace
51.61%
48.39%
100 – 199 people
6.88%
Chemicals
43.48%
56.52%
13.76%
Computers/electronics
53.85%
46.15%
200 – 500 people
Consumer goods
52.50%
47.50%
More than 500 people
16.40%
Energy
52%
48%
Food/agriculture
61.11%
38.89%
Industrial equipment/machinery
68.13%
31.87%
Mining
50%
50%
Pharmaceuticals/medical
52%
48%
Plastics
62.96%
37.12%
Textiles
68.75%
31.25%
Wood products/furniture
53.57%
46.43%
17.06% 10.59% 3.53% 6.47% 4.12% 3.53%
11.76%
$100 million – $500 million – $249 million $1 billion $50 million – $99 million $250 million – $499 million
More than $1 billion
What is the average hourly wage (rounded to the nearest dollar) for your workers on the plant floor? The average hourly wage for workers on the plant floor is $24.89. That’s almost $2.50 up from last year’s average of $22.41.
$7-14
7
$15-19
37
$20-24
$25+
31
64
For equipment purchases over the next year, which of the following production activities will be targeted? (multiple responses allowed)
42.94%
$10 million – $49 million
Hourly employee
Automotive
What is the approximate annual revenue for your firm?
Less than $10 million
3.7%
Salaried employee
What is the primary sector you serve?
How long has your company been in business?
5.20%
Human Resources
N/A
Power generation 3D printing technology Building infrastructure CNC machining/milling Moulding Welding/forming Material handling Assembling Production control Software Testing/inspection Packaging Extruding Bending/forming Stamping Sensing Mixing None Other
5.06% 8.86% 25.32% 27.85% 3.16% 20.89% 30.38% 20.25% 31.65% 43.67% 20.89% 15.82% 2.53% 11.39% 4.43% 12.03% 3.80% 4.43% 3.80%
Do you anticipate your company increasing or decreasing spending on capital equipment and technology over the next year? Decrease by around 10%
Increase by more than 10%
16.98%
20
@AutomationMag
Increase by around 10%
Increase by around 5%
No change
16.98%
28.30%
33.96%
Decrease by around 5%
1.89%
Decrease by more than 10%
0%
1.89%
November/December 2016 · MANUFACTURING AUTOMATION
STRATEGIES FOR GROWTH What is your best estimate at a dollar amount for how much manufacturing technology, software and related capital equipment and services your firm will purchase over the next year?
What information technology applications is your company currently using? (multiple responses allowed)
Less than $25,000
27.85%
$25,000 – $49,000
Enterprise resource planning (ERP)
34.38%
Product life cycle management (PLM)
8.75%
Design (CAD, CAE, CAM)
63.13%
Product data management (PDM)
18.75%
Customer relationship management (CRM) 20.63%
17.09%
12.50%
Asset management (CMMS) $50,000 – $199,000
18.99%
$200,000 – $499,000
15.19%
$500,000 – $1 million
5.70%
More than $1 million
15.19%
Warehouse management systems (WMS) 12.50% RFID systems
10%
Financial management systems (FMS)
20%
Material requirements planning (MRP)
26.88%
Manufacturing execution systems (MES)
10%
Mobile management (wireless systems)
10.63%
Supply chain management (SCM)
10.63%
Demand planning/forecasting systems
13.75%
None
10.63%
Other
1.88%
What strategic practices does your company use? (multiple responses allowed)
33.55%
48.03%
63.82%
19.08%
19.74%
20.39%
Energy Continuous Kaizen events management improvement Benchmarking Quality Total certifications productive (ISO) maintenance
46.71%
40.79%
9.87% 5.92%
Lean Maunufacturing Software integration services
Six Sigma
Agile Manufacturing
4.61%
Quick None changeover/ single-minute exchange of die
0%
Other
Unknown None other
Internally developed programs
13.16%
17.76%
Not at all important – we do not use robotics Somewhat unimportant – we use few robotics Somewhat important Very important – we strongly depend on the use of robotics Critical – robotics is integral to our operation
0%
5S methodology
Total Quality Management
7.89%
57.89%
38.16% 9.21%
17.11%
40.13%
How important is the use of robotics in your manufacturing operations?
34.21%
25.66
17.11%
Customer Value stream satisfaction mapping initiatives Supplier Recycling program management programs
What plant improvement strategies does your company employ? (multiple responses allowed)
19.08%
21.05%
3.95% 7.24%
Over the next three years, where do you plan to expand? Production
Engineering/R&D
59.33%
Where will this expansion take place?
34.67%
Sourcing
10%
10.67% Sales and service
77.55%
61.90%
We plan to reduce/contract
11.56%
36.30%
23.13%
United Kingdom
13.01% Europe
United States
20.41%
13.70% Asia
11.64% Mexico
2%
28%
5.48%
Canada
8%
Marketing
9.52%
73.97%
Unknown
45.33%
5.44% Africa
Demand from our current customers has: Increased
What regions are you most interested in acquiring customers?
No expansion planned
Decreased
6.85%
12.24% No expansion planned
Stayed the same
4.79%
South America
8.84% Australia
2.04%
0.68% other
54.67%
11.33%
MANUFACTURING AUTOMATION · November/December 2016
34% AutomationMag.com 21
YEAR-TO-YEAR COMPARISONS In the next 12 to 18 months, which is most likely to happen at your plant?
Our company’s total production has:
2016 2015 2014 2013 2012 2011 2010 2009 2008 11.81%
11.83%
14.70%
11.30%
17%
12.10%
16.30%
6.90%
17.30%
18.06%
20.85%
18.90%
21.70%
20.20%
22.90%
13.60%
10.90%
10.70%
26.39%
23.66%
25.80%
25.20%
20.60%
24.80%
22.80%
12.40%
20%
27.08%
25.35%
22.50%
24.30%
23.10%
22.10%
18%
19.80%
20%
10.42%
7.61%
9%
8.40%
9.40%
8.60%
12.90%
14.40%
12%
4.86%
6.20%
5.10%
4.60%
5.10%
5.40%
6.80%
6.90%
4%
1.39%
4.51%
3.90%
4.30%
4.70%
4%
9.50%
28.70%
16%
Increased more than 15%
Decreased less than 10%
Increased 10 – 15%
Decreased 10 – 15%
Increased less than 10%
Decreased more than 15%
No change
Contraction (layoffs)
45.95%
4.273%
Expansion
Closure
39.86%
2.70%
Merger/acquisition
6.76%
What do you see as the prime barrier to your company’s future competitiveness? Availability of skilled labour - 56.55%
Not changed
Government red tape - 21.38%
The price of our product(s) has:
Labour cost - 42.76% Work rules - 13.10%
2016 2015 2014 2013 2012 2011 2010 2009 2008 3.45%
3.10%
2.10%
1.50%
1.40%
3.50%
2.70%
2.90%
5.30%
7.59%
11.27%
8.80%
7.30%
5.40%
9.20%
9.90%
7.30%
14.70%
40.69%
32.11%
31.40%
34.30%
37.20%
39.90%
31.50%
27.30%
50.70%
44.14%
46.76%
44.50%
46.30%
44.80%
36.90%
39%
40.50%
20%
3.45%
4.79%
10.40%
7.60%
9.40%
8.10%
12%
13.70%
9.30%
0.69%
0.85%
2.10%
1.20%
1.40%
1.60%
3.10%
4.40%
0%
0%
1.13%
0.60%
1.80%
0.40%
0.80%
1.70%
3.90%
0%
Increased more than 15%
Decreased less than 10%
Increased 10 – 15%
Decreased 10 – 15%
Increased less than 10%
Decreased more than 15%
Low Canadian dollar - 24.14% Increased competition from foreign countries - 32.41% Capital investment - 17.24% Energy costs - 31.72% Cost of equipment/ automation upgrades - 31.72% Other - 2.07%
What is your company’s status relative to implementing advanced safety technologies?
36.49%
Have implemented and are fully compliant
Not changed
Have a plan and have begun implementation to comply 31.76%
8.78%
Don’t have funding to undertake implementation
Our manufacturing costs have:
22.97%
Don’t apply advanced safety technologies
2016 2015 2014 2013 2012 2011 2010 2009 2008 7.43%
7.76%
5.90%
5.40%
8.10%
7.40%
9.80%
10%
30.70%
18.92%
18.28%
18%
14.40%
20.40%
22.80%
14.80%
12.90%
16%
40.54%
39.89%
42.60%
48.60%
40.70%
38.70%
34.70%
30.60%
20%
24.32%
23.27%
19.80%
22%
18.60%
17.20%
21.20%
20.60%
8%
6.76%
7.76%
10.90%
6.50%
8.80%
11.90%
13.10%
17.20%
14.70%
0.68%
2.22%
2.40%
2%
2.80%
1.90%
4%
5.30%
4%
1.35%
0.83%
0.30%
1.10%
0.70%
0%
2.40%
3.30%
6.70%
Increased more than 15%
Decreased less than 10%
Increased 10 – 15%
Decreased 10 – 15%
Increased less than 10%
Decreased more than 15%
Not changed
Reports indicate that manufacturers are optimistic about Canada’s economic prospects over the next 12 months. When do you predict seeing improvements and/or a significant turnaround? We do not expect to see a significant turnaround.
18.62% By late 2017
7.59%
We have already experienced a turnaround.
20.69%
By the end of 2016
8.28%
By mid 2017
15.86%
By 2018
8.97% A total of 189 respondents took the survey over a six-week period in August - October 2016. The survey was emailed to our readers and the members of the Excellence in Manufacturing Consortium (EMC). 22
@AutomationMag
Beyond 2018
8.97%
By early 2017
11.03%
November/December 2016 · MANUFACTURING AUTOMATION
INTERNET OF THINGS
TAKING FULL ADVANTAGE Manufacturers who embrace IoT are leading the digital transformation BY SREENIVASA CHAKRAVARTI
T
he Internet of Things (IoT) has already transformed the world of business — offering new opportunities to compete in the market, enabling companies to change business models and creating greater insight into customer needs. While many industries have already seen massive benefits, one industry stands out as taking full advantage of IoT — manufacturing. As an industry that has been around for centuries, the rapid pace of transformation today is creating a revolution unlike anything before. Today, machines communicate with each other and with humans, and provide data for close control of the supply chain, product monitoring, and customer monitoring after products hit the market. While some manufacturers struggle to keep up with the changing technologies, others are taking full advantage of the streamlined processes, new business models and better customer service that digital transformation is enabling. A report from Tata Consultancy Services (TCS) finds manufacturers are seeing three major impacts as a result of IoT initiatives: greater insight into product quality; better customer care thanks to smarter devices; and more precise monitoring of the manufacturing process. According to TCS, more than 22 per cent of companies have implemented digital sensors to collect and return data on performance and service after products are sold and being used by customers. In fact, manufacturers are putting 35 per cent of their IoT budgets toward product monitoring. As companies track products and monitor quality more closely, customers benefit by
receiving better, more immediate customer service. TCS found more than 24 per cent monitor customer data through mobile apps and nearly eight per cent through wearable devices. While supply chain monitoring isn’t getting the most attention from the budget — about 26 per cent of most manufacturers’ total spend — it is contributing to revenue gains, and TCS predicts this will increase over the next few years. Technologies like sensors, video and software help companies keep a close watch on manufacturing, giving them greater insight into product quality and warning of any potential issues on assembly lines before time and revenue are lost.
The three stages While some manufacturers are revelling in the benefits of the new connected world, others are struggling to keep up with the ever growing number of innovations. How does a manufacturer get started? Digitalization: Digitalization is like dipping a toe in the technology pool. For example, moving a manufacturing plant’s tracking system from static charts to a technology enabled, live and dynamic system is often the easiest first step. Digital transformation: After the first taste of digitalization, there is often a hunger for more, and digital transformation is the next step. Digital transformation allows manufacturers to revamp business process and create new user experiences using technologies like mobile apps, social collaboration or predictive analytics.
MANUFACTURING AUTOMATION · November/December 2016
“Digital reimagination”: The final step is full reimagination, which allows for completely new business models enabled by technology. For example, virtual simulation allows plant operators to reimagine business processes and deliver more efficient operations by identifying critical bottlenecks in flow, understanding the behaviour of systems and deploying solutions.
What does the future hold? In the next five years, TCS predicts a shift in the way IoT budgets are allocated among manufacturers, with more money going toward supply chain and customer monitoring. In addition, manufacturers can expect IoT spending to continue to pay off in the form of improved service, enhanced products, tailored customer segmentation, targeted marketing and reduced field service costs. Among manufacturers who are in the early stages of digital reimagination, there are a few key factors to ensure successful IoT initiatives. First, companies need to outline a clear strategy that includes identifying new revenue opportunities and business models, and creating a clear plan for capturing and analyzing the data. In regards to technology, integrating IoT data with existing enterprise systems can be challenging, but if handled correctly can lead to success. Finally, embracing the new “reimagined” or connected environment requires a company-wide culture change, so introducing new technologies and explaining the need for changes throughout the process is key to acceptance. Looking ahead, manufacturers have a virtual supermarket of technologies to try, purchase and implement. The key to success is determining which technologies fit into a manufacturer’s long-term strategy and carefully planning a digital transformation. | MA Sreenivasa Chakravarti is the global head of manufacturing innovation & transformation, Tata Consultancy Services. AutomationMag.com 23
CONNECTIVITY
INDUSTRIAL COMMUNICATIONS
NETWORKS Selecting components that make the grade BY BRIAN SHUMAN
A
lmost 60 years ago, the Unimate robot kicked off an automation revolution that transformed the productivity and cost-effectiveness of manufacturing. Today, automation is expanding once again with a new model. With Industry 4.0, machines talk to machines and operations run as much on information and communications as they do on equipment and people. Critical in these “factories of the future” are communications and control solutions that deliver 24/7 network performance to support maximum productivity and minimal downtime. The first step to building reliable, high-performing communications connectivity requires understanding the conditions in those environments and selecting components that are able to withstand the rigours of industrial operations. Automation teams and their information technology (IT) partners recognize that, when it comes to communications networks, the factory floor is a very different world than typical office environments. The back office is generally clean and quiet; cables can be hidden in ceilings or under floors; and switches and other connecting components can be stored in sheltered areas. Contrast this with industrial settings where machines, automation and manufacturing equipment generate noise and vibration, and where exposure to chemicals, UV radiation, moisture and extreme temperatures are 24
@AutomationMag
likely to be the norm. These environments require a more robust communications network, built on industrial-grade Ethernet and physical assets that can withstand harsh conditions.
Building the industrial Ethernet network The difference between enterprise Ethernet and industrial Ethernet systems can best be understood by examining the impact that common, manufacturing conditions have on commercial off-the-shelf (COTS) Ethernet components. Under test conditions that simulate real-world exposure, the durability and reliability of ruggedized connectivity components quickly becomes clear. To determine how different cables hold up, three types have been put to the test: 1. A COTS Cat 5e cable with a standard polyvinyl chloride (PVC) jacket; 2. An industrial-grade Cat 5e cable with a PVC jacket; and 3. An industrial-grade Cat 5e cable with a fluorinated ethylene propylene (FEP) jacket. When simulating various environmental stressors in industrial environments, testing results have found: • Extreme temperatures: Extreme cold can make COTS cables stiff and brittle, while elevated temperatures can degrade the plastic used in the construction of cables and cause an increase in attenuation. Industrial-grade cables are proven to operate
reliably in a wider temperature range (-40 C to 85 C) than COTS cables (0 C to 60 C). • Chemical exposure: Oils, solvents, chemicals and cleaning solutions can soak into COTS cables causing the cable jacket to swell and lose mechanical strength. When cables were immersed in containers of oil and then held in a heated chamber — the COTS cable showed signs of deterioration. The industrial cable’s jacket did not, because the materials and jacket thickness are rated for exposure to oil and other substances. • UV radiation: Exposure to sunlight can cause COTS cable jackets to decompose at an accelerated rate, compromising mechanical strength and electrical performance. When cables were exposed to fluorescent UV sources that mimicked solar radiation levels for 30 days, the COTS cable jacket showed reduced tensile strength, reduced elongation and discolouration. The industrial-grade cables resisted the effects of sunlight and other UV sources and showed no
jacket damage. • Physical hazards: Industrial settings present many mechanical risks, especially for machine automation cables and connectors. Excessive machine movement or vibration can result in cables being pulled or stretched with excessive force, which can degrade performance. Plant floor vehicles can accidentally run over cables, causing abrasion, crushing or cut-through. Industrial-grade, jacketed cables have been proven to withstand up to more than a tonne of applied force without permanent damage and are less susceptible to being cut-through or losing its integrity. Armoured industrial-grade cables can withstand over a tonne of applied force without any disruption to the signal integrity. The right components ensure industrial-strength performance The cost of downtime in production environments must take many factors into account. This could include lost productivity, delayed downstream processes,
November/December 2016 · MANUFACTURING AUTOMATION
the cost of system shut-down and start-up, and the potentially devastating loss of service to customers. It’s estimated that the repair and labour costs associated with the failure of a cabling system component or Ethernet switch could be 15 to 20 times the cost of the component itself. It’s easy to see, then, how total downtime costs can quickly soar to hundreds of thousands, even millions of dollars.
IP (ODVA), Modbus Transmission Control Protocol (TCP)/Internet Protocol (IP), PROFINET and Fieldbus HighSpeed Ethernet (HSE). • Industrial-grade connectivity components, like IP20-rated or IP67-rated sealed patch cords, connectors, modular jacks and plug kits, adaptors and more. Given the potential for breakthrough advances in productivity,
quality and efficiency and the high costs associated with production downtime, it makes sense to invest in infrastructure with networking components designed and rated specifically for use in harsh and
demanding environments. The resulting integrated system will deliver the interoperability and consistently reliable performance needed everyday for years to come. | MA
Brian Shuman is a senior product development engineering project manager at the Belden Engineer Center in Richmond, Ind. He has responsibilities in the design, development, testing and technical customer support for copper cables. He is the vice-chair of the ODVA EtherNet/IP Physical Layer Special Interest Group. Additionally, he represents Belden in the TIA TR-42.9 Industrial Telecommunications Infrastructure subcommittee. He is a Registered Communication Distribution Designer through BICSI and a member of IEEE. Shuman earned a B.S.E.E. from Purdue University.
It’s estimated that the repair and labour costs associated with the failure of a cabling system component or Ethernet switch could be 15 to 20 times the cost of the component itself. Choosing the right connectivity and control components can provide a strong defence. For the physical media layer, there are many solutions available that fully conform to the IEEE 802.3 Local Area Network (LAN) standard for industrial environments, including: • Jacketed and armoured cables for extreme environments. • Continuous flex cables for use with continuous motion machines and automation systems. • Low smoke zero halogen (LSZH), water blocked and/or burial cables. • Indoor-/outdoor-rated optical fiber cabling in single-mode and multimode constructions. Many feature water-blocking agents for added protection in moisture-laden environments. • Industrial-grade Cat 5e (twopair and four-pair), Cat 6 (fourpair) and Cat 6a (four-pair) cables with heavy-duty, oil- and UV-resistant jackets. • Cables designed for use with industrial automation networking and communications protocols, such as EtherNet/ MANUFACTURING AUTOMATION · November/December 2016 MA_Yaskawa_Nov.indd 1
AutomationMag.com 25 2016-10-21 8:48 AM
COMPONENTS
HARDWIRING ALTERNATIVE UL 508 status makes connectors a viable option for wiring electrical control cabinets
U
ntil recently, an OEM which might have preferred using connectors to wire a UL 508-certified cabinet for the cost- and time-savings they offer over hardwiring also knew it probably wasn’t worth the effort. There wasn’t an absolute prohibition on their use, but the OEM was burdened with proving their safety. Obtaining that certification with connectors meant the OEM would have to submit to a lot of end-product testing. Its UL field representative would conduct a thorough safety investigation of the connector application, including the overall electrical transmission path. That added an uncertain amount of cost and time to getting a new machine to market. Most OEMs opted instead to take the path of least resistance — hardwiring all connections. Now that deterrent has been removed. Due to the longtime partnership between Harting and UL, Harting requested a new status for connectors submitted by manufacturers that pass a UL test program set up for this purpose. Those connectors become eligible for use in UL 508 applications without further testing, providing the OEM uses them as prescribed by the standards. Shifting the testing burden to the connectivity manufacturer has provided the machine builder with two practical alternatives to hardwiring: either build its own field-assembled cabinet using these pre-tested connectors, or opt for a cable assembly produced by a manufacturer, according to UL requirements, using the same components. Globally, UL 508 (508A and 508C) is not the only certification standard covering electrical control cabinet and switchgear safety, but the one most often used in North America. Substantially all industrial connectors are UL-certified for general use from the time they are introduced here, but that doesn’t pre-qualify them for use in UL 508 applications. In the UL universe, connectors 26
@AutomationMag
have been relegated to historical electrical interface categories, such as ECBT2 that use UL 1977 as their base standard. However, components for UL 508 control cabinets had to come from product groups listed in UL 508 Appendix A, “Standards for Components,” which made no provision for connectors. Now, connectors submitted by manufacturers that pass this UL testing are added to a newly created section PVVA2 of UL 2237, which was created at the request of Harting. That’s a complementary standard to UL 508 that governs multi-point connections of power cables in industrial machinery. These PVVA2 connectors bear the UL Recognized designation. Utilizing UL Recognized connectors under PVVA2 of UL 2237 fast tracks UL 508 certification of the end-use equipment since their traceability and documentation already have been established. The machine builder and end-user can count on their performance and be confident of their safety. In field assembly, these connectors must be installed by trained technical professionals following special approval stipulations, called the Conditions of Acceptability (CoA). Such requirements may contain both technical and constructive design information. For example, the power distribution cables should be selected in accordance with the TC-ER declaration and the approved wire AWG cable cross-section choices. Protective devices (fuse types RK5, CC, J or T) must be used on the cable path. The connector’s short circuit current rating (SCCR) — the level at which UL tested them — must satisfy the requirements of the cabinet. Each connector manufacturer can choose the SCCR at which to have its components tested by UL, from 5kA (the default rating) up.
UL Listed assemblies are covered by the PVVA section of UL 2237 and are identified by the manufacturer’s identification and catalogue number, model or other designation on the product or its packaging. In addition, they bear UL’s Recognized component mark. OEMs can use these connectors in pretty much any application, but there are always projects where a standard UL Listed cable assembly will do just fine and cost less. Each such assembly carries a UL certification mark, and may be employed virtually without restriction in a UL 508 application. They must be made by an approved manufacturer, have their own part number and be produced at a location specified in their UL file. The primary benefits of these connector-based alternatives to hardwiring are costand time-savings, and reliability. Hardwiring only really competes economically with connectors when a cabinet is wired once. As soon as it is unwired and rewired a second time, which often happens at some point prior to customer acceptance, the cost advantage shifts decisively to connector-based wiring. A machine large or complex enough to have an external cabinet or cabinets often is assembled and tested at the plant, disassembled for shipping and then reassembled at the customer’s location. With hardwiring, that’s a significant additional labour cost, consisting of hundreds or even thousands of dollars. Connectors are plug and play. If connector-based wiring worked at the plant, it will almost certainly work in the field from the get-go. | MA Cory Jenkins is senior product manager for Han connectors and Harting Customized Solutions.
November/December 2016 · MANUFACTURING AUTOMATION
PHOTO: HARTING
BY CORY JENKINS
NEW PRODUCTS MACHINE SAFETY Stop-time measurement service
Stainless steel safety interlock switches Omega says its K-SS Series tongue operated safety interlock switches are designed to fit to the leading edge of sliding, hinged or lift off machine guards to provide positively operated switching contacts. They offer a choice of various actuators to “aid installation and maintain durability, while providing robust position interlock detection” for moving guards, says the company. The K-SS has a rugged 316 stainless steel body and IP69K enclosure protection, and are suitable for use in food processing, pharmaceutical, packaging and petrochemical industries. www.omega.ca
emergency stop sensors with dry contacts (NO+NO or NO+NC), as well as PNP outputs from active sensors, reed switches from coded magnet actuators, and resistive inputs from safety mats and bumper switches. The relay’s output features three NO and one NC auxiliary contacts; meanwhile the relays are available in 24Vdc or 115/230Vac versions with either screw-clamp or springclamp pluggable terminations. www.wieland-safety.com
Rockford says it will offer this service for newly installed safety devices as well as for the periodic validation of existing safety devices. www.rockfordsystems.com
AUTOMATION SOFTWARE IoT device management software platform
Intelligent relays accept range of sensor inputs for machine safety Wieland Electric says it has developed a compact DIN rail mounted universal safety relay for monitoring various machine safety functions, including emergency stops, elevator access control, and heating/burner installations. The SNO4083 series of universal safety relays promise to provide “reliable monitoring” for emergency stop and noncontact protection systems for machine operators in harsh industrial environments. The safety relays accept inputs from single and dual channel
Rockford Systems has announced a “comprehensive” Stop-Time Measurement (STM) service conducted by its technicians is now available to customers using metalfabricating, metal-cutting and turning machines. STM will now be a standard service offered by the manufacturer alongside machine risk assessment, onsite machine safety surveys, and equipment compliance proposals, it says. Rockford uses STM to determine the stopping ability of customers’ industrial machinery. Once captured, the stop-time data is applied to formulas created by either OSHA or ANSI to calculate the minimum safety distance required to install safety devices.
tools. Furthermore, WISE-PaaS/ RMM 3.1 will release WISE-Agent source code as open source, notes Advantech, adding that WISE-PaaS/RMM “highly enhances” connectivity for hardware, software, devices and sensors, and helps customers to transform their business to include IoT Cloud services. www.advantech.com
Process modelling software Advantech has launched the WISE-PaaS/RMM version 3.1, an Internet of Things (IoT) device management software platform. WISE-PaaS/RMM 3.1 is an open standardized IoT software platform for users by applying MQTT, an IoT M2M protocol for device and server communication. WISE-PaaS/RMM 3.1 comes with more than 100 RESTful APIs including, account management, device management, device control, event management, system management, and database management. RESTful APIs create new web services and help integrate functions and data with their management
MANUFACTURING AUTOMATION · November/December 2016
Honeywell Process Solutions (HPS) says it has introduced the UniSim Design Suite release 450, the newest version of its process modelling software to help industrial manufacturers “increase their engineering effectiveness and optimize their process designs.” “Proven benefits of
process modelling include up to 20 per cent improvements in engineering effectiveness through best-in-class workflow tools and capital expenditure savings of up to 30 per cent through appropriate material selection in safety system design,” according to the company. With UniSim Design Suite R450, it is now possible to model multi-phase pumps (MPPs) in steady-state and dynamics, to support the evolving technology for multiphase pressure boosting, it adds. The new release includes further enhancements to the UniSim Blowdown option, which allows for the sizing and rating of blowdown networks and the selection of appropriate construction materials, in compliance with the API 521 industry standards. The UniSim Flare product, used for the sizing and rating of new or existing flare systems from relief device to the flare tip, has been re-platformed and enhanced for “better performance, data visualization and reporting, and scenario automation.” www.honeywellprocess.com AutomationMag.com 27
NEW PRODUCTS MOTORS & DRIVES Gearboxes offer “quiet startup and smooth operation”
AutomationDirect’s IronHorse line of motor products now includes helical gearboxes which promise to provide “quiet startup and smooth operation” in applications such as conveyors, packaging machines, rotary tables and more. Designed for use with 1Hp to 20Hp
electric motors, IronHorse gearboxes reduce output speed while increasing torque, says AutomationDirect. The gearboxes feature C-face and TC-face inputs, inline outputs, and are available in five frame sizes ranging from 56C up to 254/6TC with six nominal ratios of 5:1 to 60:1. They are constructed of FC20 cast iron one-piece housings, and feature a carbon steel shaft protected with shaft sleeves, as well as heat-treated and ground high-strength steel gears. www.automationdirect.com
NEMA 34 frame size Applied Motion Products has added the NEMA 34 frame
ROBOTICS Design a robotic handling system with this configurator
Festo says an engineer can design an electric robotic handling system for a machine or process in “as little as five minutes” with the help of its Handling Guide Online (HGO). According to the company, it has simplified the design process for systems like slides and gantries by modularizing components based on an analysis of more than 700 different project applications. The web-based HGO, using data keyed in by the customer, draws on this pre-defined, standardized content, to create the “optimal solution” for his or her application. Rather than having to select and size individual components, the customer is prompted by the HGO to provide data describing the application requirement. Then 28
@AutomationMag
he or she adds data such as the weight of the payload to be moved, the type of axis, working stroke, motor position, etc. When the design is completed, the customer can download the CAD model and data sheet for immediate use, without charge. Festo then sends the customer a net quote for the device. www.festo.com
Robotic platform strives to maximize customer efficiency
Fives Liné Machines says its Liné Machines Robotics platform will complement the traditional, large machine tool solutions already being provided to the aerospace, rail and heavy equipment industries. The solutions will focus on: milling, trimming and drilling; deburring and polishing; cleaning and surfacing; forming inspection and scanning; automation, tooling and part holding; and peripheral equipment for machine tools. www.fivesgroup.com
size to its StepServo integrated motor family. The addition of the larger frame size in the
product offering represents a “widening of the product range,” says the company, which already includes smaller frame sizes NEMA 11, 17, 23 and 24. According to Applied Motion Products, the NEMA 34 frame size means the motors can now be installed in more demanding applications where greater torque is required. TSM34 and TXM34 StepSERVO integrated motors come in four lengths; the longest motors (-6) offer holding torque values of 1,161 oz-in (8.2 N-m) and peak torque values over 1,300 oz-in (9.2 N-m). TXM34 integrated motors are IP65 rated with M12 connectors for all connections and a shaft seal at the front shaft. TSM34 integrated motors are IP40 rated with screw terminal and pluggable connectors for power, communication, and I/O connections. A highly anticipated feature of the NEMA 34 StepSERVO Integrated Motors is dual-port Ethernet, which simply means two Ethernet ports per motor instead of one. The motors can now be daisy-chained in a line network topology in addition to the traditional star network topology. This small improvement allows for cost savings and design simplification via the reduction of cable lengths, the omission of bulky cable runs, and the downsizing of network switches, it says. www.applied-motion.com
Gearheads with helical gearing Harmonic Drive adds Harmonic Planetary HPG gearheads with helical gearing and low reduction ratios to its current planetary gearhead lineup.
The new model, HPG-R, add low-speed ratios from 3:1 through 10:1 including all integer ratios in between. HPG-R employs helical gearing for improved noise reduction and higher torque capacity, says Harmonic Drive, adding that the gearheads are “ideal” for a variety of machinery and equipment designs. The design of the HPG internal gear allows a preload of the gear (on the order of microns) and enables it to “slightly deform elastically thus maintaining low backlash for the life of the gearhead, without any need for adjustment,” it says. This preload not only minimizes backlash but also compensates for interference between meshing parts, it notes. The HPG-Helical gears also feature Quick Connect coupling for “easy mounting.” www.harmonicdrive.net
Direct drive linear motor
The SDLM-025-070-01-01 direct drive linear motor from Moticont, also known as an electric cylinder, boasts a built-in encoder, zero backlash, zero cogging, and provides users with “high acceleration, high speed, high resolution, and long life.” The motor features 1.25 µm (0.000049 in.) in of resolution, and offers a stroke length of 0.500 in. (12.7 mm), a continuous force rating of 22.2 oz. (5.9 N) and peak force of 67.2 oz (18.7 N). Both ends of the motor and shaft ends are drilled and tapped for “easy” integration into new and existing applications. According to Moticont, suitable applications include manufacturing, semiconductor handling, inspection, and door and valve actuators. www.moticont.com
November/December 2016 · MANUFACTURING AUTOMATION
MATERIAL HANDLING Drive platform for material handling
Siemens has released the Sinamics G110D drive platform, describing it as “ideal” for installing in close proximity to motors located throughout facilities where dust and water ingression are a concern. According to the company, the G110D combines “improved functionality, increased energy efficiency, a smaller footprint, lower total cost-of-ownership
and enhanced usability” in a single drive. It also features integrated plug-and-play power and control, optional Intelligent Operator Panel (IOP) for “simple” text application setup, alarm status alerts and resolution advice, optional power disconnect switch and IP65 metal housing enclosure. Applications for the platform range from material handling, packaging conveyors, airport baggage carousels to pumps, fans, compressors and other industrial equipment. www.usa.siemens.com
Mobile-friendly website The mobile-friendly website from Anver is now live, offering
PROCESS CONTROL Solution for process applications
Rockwell Automation says its SequenceManager solution enables “powerful and flexible” sequencing capabilities of the batch process at the controller, offering “increased
functionality” for skids, off-network systems and single-unit controls. Leveraging a Logix-based controller platform, the solution allows operators to configure, view and obtain information about batch sequences stored in the controller, says Rockwell, adding that it will increase visibility and accessibility to all stages of the production process. According to the company, the solution is suited for single- or multiple-independent unit operations. www.rockwellautomation.com
a “responsive design” that works on desktop, mobile, and tablet devices to view product information, videos and other resources. The new mobile format automatically resizes text, images, and videos and rearranges navigation to best fit the device on which it is displayed, says Anver, adding that the decision to create
a mobile-responsive design is due in part to an effort to provide customers with the “best possible online experience and to stay current with the latest technology.” The mobile site aims to “closely reflect” the company’s full desktop version in terms of design and functionality. www.anver.com
ADVERTISER INDEX Allied Electronics Inc. 1,11 AutomationDirect 2 Beckhoff Canada 5 Eaton Canada 13 Encoder Products Company 6 Fluke Electronics 15 Harmonic Drive LLC 17 Hiwin Corporation 9 Murrelektronik Canada 3 SCHUNK Intec Corp. 31 SEW-Eurodrive 29
Siemens Canada Ltd. 32 TURCK Chartwell Canada Inc. 7 WESCO Distribution Canada LP 8 Yaskawa America, Inc. - Motoman Robotics Division 25 TO ADVERTISE Contact Klaus B. Pirker kpirker@annexweb.com
ManufactAuto-May2016.pdf 1 17/05/2016 3:59:34 PM
C
M
COMMUNICATIONS & NETWORKING “Feature-rich” switch family Microsemi, a provider of semiconductor solutions, has announced its Ocelot product family, describing it as a “low power, feature-rich” Ethernet switch family optimized for communications networking in the industrial Internet of Things (IIoT) market. Designed for the specific needs of industrial Ethernet switch applications, such as factory automation, process control, smart grid/ smart energy and physical security, the devices promise to
Y
CM
simplify IIoT network migration to an Ethernet backbone with “flexible interfaces,” TCAM based classifications, 1588 timing and ring protection in a “small package.” The Ocelot family includes: VSC7511, a four-port, layer 2 gigabit Ethernet switch with four fully integrated copper PHYs; VSC7512, a 10-port, layer 2 gigabit Ethernet switch with four fully integrated copper PHYs; VSC7513, an eight-port, layer 2/3 gigabit Ethernet switch; and VCS7514, a 10-port layer 2/3 gigabit Ethernet switch. www.microsemi.com MY
CY
CMY
K
MANUFACTURING AUTOMATION · November/December 2016
AutomationMag.com 29 MA_SEW_MayJune.indd 1
2016-05-18 2:59 PM
BACKSTORY WHAT WE PUBLISHED IN... 1998 “The Webenabled factory: Current and near-future implications of Internet technologies on automation devices.”
2011 “UBC and Toyota receive federal funds to re-invent wheel manufacturing.”
2001 “Running a manufacturing company with yesterday’s technology and mindset — such as epitomized by Material Resource Planning (MRP) — cannot succeed in the long term.”
2013 “Embracing 3D printing technology could revolutionize the modern industrial plant.”
2008
Updating aging infrastructure is good for business
A
legacy built from years of service, excellence and reliability is an asset to any company, but leveraging the long-standing relationships with partners and loyal customers built from that legacy can be the key to success in the manufacturing industry. However, when it comes to technology, an over-reliance on the past can be the quickest way to derail the future. Running a business on the stamina of an outdated, aging technology infrastructure is possible, but running a modern, successful business requires a modern IT strategy. For organizations looking to update aging infrastructure, it may seem like a daunting task as there was likely a considerable investment — both time and money — in the current system, and the thought of selecting, implementing and learning an entirely new
30
@AutomationMag
business management or enterprise resource planning (ERP) system probably leaves you feeling anxious. Not only will you have to devote some time to sourcing a new system, you’ll also have to make a case to the internal team as to why the company should invest in it. The good news is that technology has advanced since your last implementation. Systems are intuitive, competitive and with the right support, updating from legacy software can be a quick and easy process that does not have to result in any downtime or business interruptions. We live in the era of digital data where it can be mined for valuable insights to save a company time and money. If you’re relying on a legacy ERP system or error-prone spreadsheets for inventory and accounting, you might be missing out on actionable data that could help
“There’s a new technology in manufacturing that has the potential to be a game changer for our industry.” 2014 “The reality is that using paper or collating numbers on an Excel spreadsheet to collect performance information will always leave factories with data that is subjective and out of date.”
you make better informed business decisions. While modern solutions organize and analyze data, they can also proactively solve identified problems by creating a more efficient and knowledgeable operation. Whether you need recall management, inventory forecasting, formula management, or capacity planning, there are tools available to meet your needs. Technology has advanced so that it can be custom tailored to the unique needs of each business. Options are available to suit the needs of companies, whether you want to expand into other markets, seek real-time control of production planning and insight into regulations, or strive to effectively manage the fluctuation of procurement, production and shipping while staying on top of compliance requirements. | MA Mike Wingrove is vice-president North American sales at Sage North America, a provider of business management software and services. Visit bit.ly/1ZUDs0X to read the extended version of this article.
November/December 2016 · MANUFACTURING AUTOMATION
Š 2016 SCHUNK INTEC, Inc
SCHUNK grippers. Proven since 1983
High tech from a family-owned company
The new SCHUNK Grippers PGN-plus-P und PGN-plus-E of the
With more than 4,000 standard components, the most extensive line of robust and durable small component and universal grippers sets worldwide standards in all industries.
Generation Permanent With lubrication pockets in the multi-tooth guidance.
25% higher gripping force. SCHUNK miniature parallel gripper MPG-plus pneumatic. Jens Lehmann, German goalkeeper legend, SCHUNK brand ambassador since 2012 for precise gripping and safe holding.
Closing time:
0.03 seconds. SCHUNK 2-finger small component gripper EGP 25-Speed, electric.
Easiest integration. SCHUNK 2-finger long-stroke gripper EGA, electric.
The flexible drive system for high-performance motion control applications Machines must be manufactured cost-effectively and should offer end-users more productivity. The Siemens SINAMICS motion control drive system addresses both needs.
The modular SINAMICS drive system addresses demanding applications in plant and machinery construction. Single and multi-axis drives offer high dynamic performance with integrated comprehensive functionality and a scalable number of axes for almost any drive application. The sophisticated functionality of SINAMICS drives facilitates new and innovative machine concepts and significantly increases production yield. For information, call 1-888-303-3353.
siemens.com/sinamics