October 2026 SUBSCRIBE FOR FREE
www.engineerlive.com
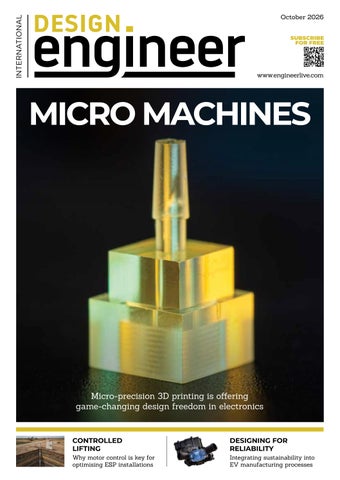
MICRO MACHINES
Micro-precision 3D printing is offering game-changing design freedom in electronics
CONTROLLED LIFTING
DESIGNING FOR RELIABILITY
Why motor control is key for optimising ESP installations
Integrating sustainability into EV manufacturing processes
+25,000 Springs
Lee Spring Benefit
About Lee Spring
25,000+ products available, plus custom products made to your specification. • Springs ready to ship today. • Experienced engineering and design assistance.
Trusted global spring manufacturer since 1918. ISO 9001:2015 certified with worldwide locations.
sales@leespring.co.uk +44 118 978 1800 Unit 2, Smallbridge Industrial Park, Riverside Drive Rochdale, OL16 2SH leespring.co.uk
CONTENTS
Welcome As Europe leaves the heatwaves of the summer behind in favour of cooler weather, many of us will breathe a collective sigh of relief. As we reflect on the extreme temperatures of the last few months, it’s clear that industry has a more crucial role to play than ever in reducing emissions and their impact on our environment. Many companies continue to work hard towards this aim, from integrating sustainability into vehicle manufacturing processes early on (page 12) and reducing vehicle weight with energy-efficient composites (page 34), to improving sustainable operations in facilities (page 32) and optimising ESP installations (page 44). Flexibility is also a key talking point in this issue, led by our cover story (page 6) which explores how micro-precision 3D printing is offering electronics design engineers greater freedom. Elsewhere, we look at how connector seals can improve design flexibility in battery platforms (page 13) and hear how rethinking power design creates new options for engineers (page 24). AI continues to grab headlines across all major industries. This issue discusses the engineering case for open architecture and edge AI (page 19) and new possibilities for quantum computing operations (page 23). On page 47, we evaluate Europe’s next phase of digitalisation. As always, turn to page 50 for the latest skills and training updates across design engineering, and page 52 for the upcoming industry events you need on your radar. Hayley Everett Editor
6
OCTOBER 2026 COVER
6
ADDITIVE MANUFACTURING
Micro machines How micro-precision 3D printing solutions are offering electronics design engineers greater freedom
14
From the lab Rounding up the latest 3D printing research breakthroughs
AUTOMOTIVE DESIGN
INSTRUMENTATION • ELECTRONICS
10
16
Keeping cool
12
Why thermal management is an overriding design priority for commercial vehicles
Designing for reliability
13
Semiconductor supply
19
Unpicking Avnet Silica’s latest Trendliner report
Unlocking edge AI The engineering case for open architecture
Integrating sustainability into EV manufacturing processes from the start
Flexible connection How connector seals improve design flexibility in battery platforms
14 www.engineerlive.com
3
CONTENTS
23
Coupling qubits MIT’s new qubit architecture is enabling faster, more accurate quantum computing operations
24
Rethinking power design Integrated power ICs create new options between prequalified modules and fully discrete power architectures
FASTENERS & SEALING
SHOW PREVIEW
39
52
Structural bonding Considerations for selecting structural adhesives for performance and production
42
Handle it Overhauling the design of free-fit hinge pins for medical device handles
Frankfurt am Main from 17–20 November
Industrial AI in focus
at SPS
SPS takes place in Nuremberg from 24–26 November
MATERIALS • PROCESSES • FINISHES
26
Self-healing vehicles How well do self-healing materials really work?
29
Coating conditions Why assessing coating
32
performance begins long before the first coat is applied
MOTORS, DRIVES & CONTROLS
44
Controlled lifting Why motor control is the
47
phase of digitalisation
A specialist finish We visit Plastic Coatings' Kingswinford 24-hour processing facility
COMPOSITES
34
Lighten up Helping aeronautics
37
and transport vehicle manufacturers reduce weight and improve energy efficiency
Composites take flight How tomorrow’s air travel will
Showcasing Turkey’s composite sector TURKCOMPOSITE welcomes the composite sector from 21-23 October
key starting point for optimising ESP installations
Simple advantage Evaluating Europe’s next
SKILLS ZONE
50
M takes centre stage A in Frankfurt Formnext returns to
Connecting innovation with industry Advanced Engineering returns to the NEC from 4–5 November
Growing graduates Meeting increased demand
51
for engineering skills across critical infrastructure
Electronics engineers in demand Five ways electronics employers can attract the next generation of talent
depend on composite materials
39
PUBLISHER Jerry Ramsdale EDITOR Hayley Everett heverett@setform.com DESIGN – Dan Bennett, Jill Harris HEAD OF PRODUCTION Luke Wikner production@setform.com HEAD OF SALES & PARTNERSHIPS David Pattison ACCOUNT DIRECTORS John Abey | Peter King SENIOR ACCOUNT MANAGERS John Davis | Darren Ringer | Roy Glasspool ACCOUNT MANAGERS
4
Setform’s international magazines for engineers are published quarterly and distributed to senior engineers throughout the world. Other titles in the company portfolio focus on Oil & Gas, Design, Transport, Mining, Energy and Power. The publishers do not sponsor or otherwise support any substance or service advertised or mentioned in this book; nor is the publisher responsible for the accuracy of any statement in this publication. ©2026. The entire content of this publication is protected by copyright, full details of which are available from the publishers. All rights reserved. No part of this publication may be reproduced, stored in a retrieval system, or transmitted in any form or by any means, electronic, mechanical, photocopying, recording or otherwise, without the prior permission of the copyright owner.
Paul Maher | Iain Fletcher | Marina Grant
Setform Limited | Suite 3.10, Ellisse by Spacemade, 10 St Bride Street, London EC4A 4AD
e advertising@setform.com
t +44 (0) 207 253 2545 e mail@setform.com
www.engineerlive.com
MICRO MACHINES Micro-precision 3D printing is offering game-changing design freedom in electronics
17 – 20.11.2026 FRANKFURT / GERMANY
Where Additive Manufacturing Advances Your Production Discover how Additive Manufacturing enables more efficient, flexible, and sustainable industrial processes while making your production more independent and cost-effective. Gain clear guidance for investment and strategic decisions through direct exchange with leading providers and users. At Formnext, international market leaders showcase the latest developments across the entire AM process chain – from materials and manufacturing systems to automated post-processing, as well as software and quality assurance solutions. Secure your ticket now!
formnext.com/tickets
Honorary sponsor
Messe Frankfurt Group
COVER STORY
MICRO MACHINES Micro‑3D printing produces liquid connectors with sub‑millimetre internal geometries
Jake Collins explains to Louise Davis how micro-precision 3D printing solutions are offering electronics design engineers game-changing levels of freedom
6
www.engineerlive.com
COVER STORY
O
ne of the things Jake Collins finds particularly satisfying about his work is its lack of constraints. Collins is senior applications engineer at Boston Micro Fabrication, a USheadquartered manufacturer of micro-precision 3D printers. He describes the freedom that micro-precision 3D printing brings enthusiastically. “When you look at conventional manufacturing processes, they have built-in ‘rules’ that engineers and designers have learned to work within and those constraints on the process dictate how a part can be designed,” Collins begins. “Consider design limitations on mould cavities and CNC machining as examples. Both of these processes are great manufacturing techniques for many products currently out in the world but they may limit an engineer on how they can design a part – whether it’s avoiding internal overhangs that can’t be moulded or machined, or wall thicknesses below a certain size due to tool sizes,” he adds. Collins points to a 3D printing technique called projection micro stereolithography (PµSL) as the way to remove many of those sort of constraints. “It builds parts voxel [volumetric pixel] by voxel and layer by layer, allowing for extremely high dimensional control as well as no restrictions from conventional processes, such as a mould-pull direction or directional paths of cutting tools,” he explains. “What this gives us is true control over 3D routing of channels and interconnects in electronic components, as opposed to planar or layered routing from limitations in manufacturing. It also allows for geometry that would be unmanufacturable previously – such as a latticed section within a part – that mould tools and conventional machining would not be able to do. PuSL enables engineers and designers to design for function, not around the manufacturing processes that constrain the design traditionally,” Collins emphasises.
GRAND DESIGNS
Removing longstanding design constraints is an important part of helping designers to meet the
While micro injection moulding takes 10-12 weeks for critical components, 3D printing offers faster production and greater flexibility in design
challenges associated with today’s trend for electronic devices becoming ever smaller and more complex. On this, Collins observes: “Because of its design freedoms, additive manufacturing allows for a shift in thought processes from assemblybased design to a performance-based design. Traditionally, all components would be manufactured separately (using separate processes due to constraints on the manufacturing process) and then assembled into the final part. This introduced additional labour, tolerance stack-ups and more failure risk. Now with micro-additive manufacturing, part consolidation is possible and end parts can be
designed as a single structure that combines many of these aspects.” The engineer notes that although this process may not replace every single component in every material, as some perform specialised tasks, consolidating a number of components can help to maximise performance and minimise risk of failure through multiple modes. “For example, looking at fibre arrays since they are a high-priority type of part with data centres, a printed fibre array guide could introduce a very close-packed spacing between fibres at very high tolerance, while also allowing for internal direction change and tapering the bore
Jake Collins, senior applications engineer, BMF
Removing longstanding design constraints is an important part of helping designers to meet the challenges associated with today’s trend for electronic devices becoming ever smaller and more complex www.engineerlive.com
7
COVER STORY
Injection moulding and precision machining get harder and more expensive as features shrink, but micro 3D printing maintains exacting precision
geometry and size,” Collins details. “This can provide lower signal loss and allow directional changes that would be impossible with traditional methods. Being able to pack more fibres into a space and route more efficiently could allow for higher performance and smaller end parts.” He adds: “Other examples of parts we have already seen include embedded fluid channels for thermal management, as well as creating vertical interconnect accesses (VIAs) through selective metallisation, which would require a much more complex
Micro-precision 3D printing enables complex 3D microfluidic channels for rapid design validation
8
www.engineerlive.com
approach or even be impossible to manufacture via other methods.”
ARCHITECTURAL DIGEST
Rather than only making things smaller, Collins believes that microprecision 3D printing could also enable electronics designers to rethink traditional architectures entirely: “As we have advanced further we have definitely become more complex and pushed towards miniaturisation of devices and components across many industries. Miniaturising existing
architectures relies on the same thought process of designing around limitations that may have been present when creating the existing design. Micro-additive asks a different question: if you weren’t constrained by existing manufacturing methods (i.e. planar PCBs, discrete connectors, etc.) what would you actually design?’” Expanding on this, he says: “Looking at it from that point of view allows engineers to approach the problem they are trying to solve in a different way. Some ideas we think could be interesting in the future include designing based on 3D electronics, not a stack-up of 2D boards. Using interconnects that run through the extents of the part in X, Y and Z without limitations allows for more natural routing; think vasculature of blood vessels instead of rigid 2D stacks.” Collins cites the use of specific connectors and interposers for an exact application as another example here – essentially custom parts per design instead of using the more standardised designs that are often used today purely because they’re more readily available. “As you push into the smaller sizes of parts, such as sub-mm fibre and sensor arrays, there aren’t as many off-the-shelf parts available and creating custom designs allows for capture of those incremental performance gains,” he explains.
COVER STORY
CASE IN POINT
BMF worked with Horizon Microtechnologies on corrugated horn antennas for millimetre-wave systems
AREAS OF INTEREST
When asked which areas of electronics design he thinks could be most fundamentally transformed by microprecision 3D printing, Collins uses lessons learned from current successes to inform his future predictions, “A few of the different sectors that can be transformed by micro-additive are ones that already have been, to some extent,” he observes. Photonics and interconnects are top of this list. Colins says: “Fibre alignment, coupling and packaging require exacting tolerances and smaller and smaller features, which lend themselves extremely well to micro-additive. Building on that, complex 3D channel geometry – such as tapered/bored, internal routing changes and HCP arrays – all of which micro-additive is uniquely good at, are giving higher performance and expanding that industry further.” The expert cites radiofrequency (RF) and microwave components as another key area. “This has been a space we’ve been involved in for a while because microadditive allows for 3D antenna and waveguide geometries that just wouldn’t be possible with traditional manufacturing, and these new parts are designed to outperform the planar geometries. Our customers can quickly produce end-use parts that
outperform traditional planar parts.” As well as those industrial applications, Collins highlights consumer micro-devices as a significant application area – particularly hearing aids, smart glasses and wearable sensors. “All of these are designed to be minimally invasive and blend in seamlessly with the wearer, so creating smaller, more precise versions has been a big goal in the industry,” he says.
FREE TO CHOOSE
Regardless of the type of application, Collins says that the overall message he’d like to share is that microadditive manufacturing isn’t just about ‘printing small stuff faster’. Rather, he notes, “It’s that it enables design freedom and delivers complexity for free for designers, so their focus can be on the application and performance, rather than the constraints of manufacturing.” “It also allows for faster and cheaper design cycles, giving engineers more time and flexibility to test new designs without the fear of failure from time and cost in traditional methods. As devices and electronics get smaller and require higher performance, micro-additive manufacturing can change the rules and open new ways to tackle these challenges,” Collins adds.
One real-world example of the design freedom microprecision 3D printing delivers can be found in the work of one of BMF’s customers, Horizon Microtechnologies, which specialises in RF solutions. “We worked with their team on some corrugated horn antennas for millimetre-wave systems. These are a pretty typical type of design, but the internal geometries (the corrugations) that give it high performance are typically hard to manufacture,” explains Collins. “As you move into higher frequencies, there is an inverse relationship with feature size, and the features become smaller and require higher tolerances. With the scale required for high-frequency applications, typically a few hundred microns, traditional machining runs into limits and requires multiple parts to even produce, which adds the possibility of alignment error. Using the micro-additive manufacturing approach, the entire horn geometry was produced as a single part,” he details. From there, Horizon applied its proprietary conformal metallisation process directly to the printed part, which allowed for full metallisation through the corrugated grooves at extremely high precision. Collins comments: “This hybrid approach resulted in shorter lead times, more freedom of design (so potentially higher performance) and minimised RF losses, as the part has minimal surface roughness and no parts to assemble and introduce alignment error. This shows that micro-additive isn’t just a prototyping option; companies are already using it to produce high-performance end-use parts while avoiding the constraints of traditional manufacturing.”
www.engineerlive.com
9
AUTOMOTIVE DESIGN
KEEPING COOL Chad VanRens explains why thermal management is an overriding design priority for commercial BEVs and FCEVs TLX’s 4-way switching valve
E
-mobility platforms continue to proliferate well beyond the passenger vehicle market. Logistics companies are increasingly electrifying their fleets, especially for urban logistics and last-mile fulfillment. This is driving the development of BEV and FCEV commercial vehicles and yard tractors. Thermal management is an overriding design priority for these vehicle architectures. The cooling systems in these vehicles are far more complex than what are found in typical ICE vehicles. ICE thermal management systems are more focused on rejecting unwanted heat. But e-mobility platforms have more complex thermal requirements and also employ systems that retain, recycle, or even generate heat to keep vital components within their proper operating temperatures. Because new e-mobility platforms are constantly being developed, OEMs often have to develop new components to meet thermal
10
www.engineerlive.com
management needs. This has led to a somewhat surprising trend when it comes to thermal management valves.
VITAL VALVES
Across an OEM’s platforms, there may be a need for valving solutions that are similar but not exactly the same. This can drive OEMs to rely on multiple vendors to supply closely related components, complicating their supply chains and increasing their costs, costs which are inevitably passed on to their customers. TLX Technologies took notice of this trend when it began receiving inquiries for different valves with similar performance characteristics. The company decided to develop a modular solution that allowed OEMs to change
key specifications without altering performance. This approach eliminates the need to develop an entirely new valve concept for each variation. The intent was to give OEMs and system suppliers a single valve concept that would work across multiple vehicle platforms. This keeps buyin costs to a minimum and reduces project risk because data from prior durability and performance testing can be leveraged for each variation.
MODULAR MOBILITY
TLX’s modular valve product family is the result of that effort. This product family currently includes a threeway switching valve and a four-way switching valve. These high-flow valves can be specified with port sizes up to
The intent was to give OEMs and system suppliers a single valve concept that would work across multiple vehicle platforms
AUTOMOTIVE DESIGN
Electrified work trucks are proving their capability, expanding the reach of BEV and FCEV platforms into heavy-duty and off-road applications
25.4mm, without making any changes to the internal flow paths or diverter. The valves also meet the power and control requirements of differing platforms by supporting both 12 and 24 Vdc operation and offering a choice of communication protocols with feedback. If the required feedback is a simple fault error, then OEMs can choose PWM. If they require specific fault codes for conditions like overcurrent, motor stall, motor stall lockout, overvoltage, undervoltage, or overtemperature, they can choose LIN. While not yet available, TLX is currently considering adding CAN communication for future revisions. TLX also understood that its flow control valves would have a downstream impact on the overall performance of the thermal management system. The valves needed the right performance characteristics to ensure that the system’s energy and thermal efficiency are enhanced instead of hindered. The company tackled that
challenge through three key features. First, these valves maintain diverter position without drawing any current. This means the valve itself has minimal impact on the vehicle’s electrical budget. Second, the flow paths are designed with gradual turns and smooth transitions, which minimises pressure drop. This means the pump is more easily able to handle fluid circulation demands while using less power. Third, these valves minimise cross-flow leakage. Leakage across the flow paths at the diverter can cause thermal inefficiencies and drive the need for larger coolers, heat exchangers, and pumps. By keeping cross-flow leakage low, the system is more predictable and controllable and can utilise more efficient components within the coolant loop.
REDUCING CONSUMPTION
Together, these features help reduce the thermal management system’s
energy consumption and improve its overall thermal efficiency. This results in better range, which is not only important for passenger vehicles but is particularly so for commercial applications, where taking a vehicle out of service to charge can negatively impact operations. The improved thermal control also contributes to the increased longevity of temperaturesensitive components like the traction battery, power inverter, and motor. TLX’s modular valve product family is also designed to meet the demands of continually evolving thermal management systems. The architecture of these valves is adaptable to changing flow control demands, with a three-way proportional valve, a two-way switching valve, and a twoway proportional valve as the next likely configurations.
Chad VanRens is at TLX Technologies: www.tlxtech.com
www.engineerlive.com
11
AUTOMOTIVE DESIGN
DESIGNING FOR
RELIABILITY A new case study from Hottinger Brüel & Kjær demonstrates how sustainability can be integrated into electric vehicle manufacturing processes from the start
The EV manufacturer aims to accelerate the global transition to sustainable transportation
L
aunching a new electric vehicle (EV) company is fraught with challenges, not least proving long-term product reliability without historical data, and building credibility in a competitive market. This is the problem Hottinger Brüel & Kjær’s (HBK) customer faced, as a new American EV manufacturer that designs and manufactures electric adventure vehicles, commercial delivery vehicles and its own charging infrastructure.
ESTABLISHING TRUST
Unlike legacy car manufacturers, HBK’s customer didn’t have a longstanding reputation of decades of field data to back it up. This means each product needed to prove its reliability from day one and build critical brand loyalty quickly. The company’s adventure vehicles must withstand extreme environments and temperatures, which place immense stress on the chassis, battery, suspension and propulsion systems. Integrating novel quad-motor propulsion – a large and complex battery pack – also posed a challenge, as did the company’s
12
www.engineerlive.com
sophisticated software-defined architecture that created countless potential failure modes.
ENTER HBK
To meet these challenges, the EV manufacturer established a dedicated Design for Reliability (DfR) department, which embedded HBK’s ReliaSoft suite as its core toolset to build its products. Before physical testing begins, ReliaSoft is used to design statistically robust test plans, including Accelerated Life Tests (ALT). These tests enable the company’s engineers to determine the exact number of samples, stress levels and test durations required to prove a component will meet its life target. As data comes in from lab testing and customer fleets, it is fed into HBK’s Weibull++ tool, which analyses the data to create precise models of a component’s expected life. Using HBK’s BlockSim tool, the engineering team can model an entire vehicle as an interconnected system. By inputting the lifetime predictions for individual components from Weibull++, the team simulates the
overall vehicle reliability and identified which components had the biggest impact on system-level performance. Throughout the design process, HBK’s XFMEA tool is used to systematically identify potential failure modes and their effects, allowing the engineering team to address risks digitally.
FUTURE FOUNDATION
Integrating a standardised DfR programme with ReliaSoft not only delivered early insights into lifetime performance of components, but also provided a 9% improvement in product development efficiency. By using accelerated testing and predictive models, the EV manufacturer could identify and fix potential weaknesses much earlier in the development cycle. System modelling also prevented over-engineering on non-critical parts while ensuring the systems essential for safety and adventure were robust. The ability to analyse customer fleet data enabled the manufacturer to create a continuous feedback loop based on real-world data, making future product designs more durable and customer-focused.
AUTOMOTIVE DESIGN
FLEXIBLE CONNECTION
How connector seals can improve design flexibility in battery platforms
W
ith battery technologies shaping key aspects of modern life – from electromobility to energy storage systems – modern battery packs must meet increasingly demanding requirements for mobile, safe and efficient provision of energy. To meet this need, Freudenberg Sealing Technologies has developed a customer-specific, configurable connector seal concept that supports new system-level approaches in modern battery packs. These components are based on multifunctional, modular cell connector plates for cylindrical, prismatic or pouch cells, manufactured to customer specifications from nickel-plated or tin-plated copper and overmoulded with elastomer. In addition to offering high levels of electrical insulation, the elastomer components meet all requirements of
modern battery systems. Depending on the customer’s technical specifications, it is possible to directly integrate different seals and seal geometries – such as housing seals, cell seals or other protective features. Additional functional integrations enhance the component’s value and create a cell connector that provides not only its electrical function but also offers significant advantages in terms of assembly, installation space, robustness, damping and system integration within the battery pack. Functions that were previously handled by separate components for contacting, sealing, insulation and mechanical guidance are now combined in a single concept. This reduces interfaces, shortens tolerance chains and minimises potential failure risks. Freudenberg Adhesive Clean Technology (FACT) complements the concept of the connector seals
The configurable connector seal concept
as a clean and efficient bonding system. It enables the elastomer to be permanently adhered to the cell connector surfaces, which typically resist bonding. Eliminating the conventional wetchemical pretreatment offers the benefits of a resource-conserving manufacturing process and reduced dependence on bonding agents in the supply chain, while enabling almost complete design freedom for the connector. For customer-specific battery applications, this allows for a targeted approach to different cell formats, pack architectures and requirements.
INNOVATION THROUGH COLLABORATION FROM DESIGN THROUGH PRODUCTION,
© 2026 TLX Technologies
TLX Technologies works hand in hand with your design team to develop and produce custom solenoids and valves for your most challenging applications.
CONTACT US WITH YOUR CHALLENGE
sales@tlxtech.com | tlxtech.com
www.engineerlive.com
13
ADDITIVE MANUFACTURING
FROM THE LAB Rounding up the latest additive manufacturing research breakthroughs in robotics and adaptive materials
The MICROBS Lab’s microflier
W
hile recent years have seen the global additive manufacturing industry shift its focus towards industrialisation, the importance of research and development (R&D) projects remains crucial in opening up new possibilities and applications for the technology. Research spending in areas such as defence and AI, for instance, have increased significantly in the last few years. Private investments in start-ups and spin-outs continue to scale up, too, as the industrial case for many of these technologies strengthens. Here, we take a look at some of the latest innovations in additive manufacturing R&D across the globe.
MINI DRONES
EPFL engineers have designed acoustic cavities that convert sound waves into thrust, propelling small robots and ultralight aerial vehicles without on-board actuators or electronics. The team in EPFL’s MicroBioRobotic Systems (MICROBS) Lab harnessed the physics behind the Hemholtz resonance phenomenon, which occurs when airflow passing across an opening causes air trapped inside a
14
www.engineerlive.com
Using category theory to break a pine cone’s humidity response into independently validated building blocks. Image via MIT
cavity to oscillate back and forth. “Instead of pushing devices around with sound waves, we have created acoustic resonators that are tuned to harness sound at specific frequencies to generate directional thrust and controlled motion,” says lab head Selman Sakar. “Our work shows the feasibility of transforming a simple, cleverly designed mechanical piece into robotic matter.” Using a 3D nanoprinting technique, the team built ‘microfliers’: ultralight flying vehicles with three microscopic cavities integrated directly into their polymer structures. One design weighing just 150 micrograms used its cavities to generate direct upward thrust like a rocket. Another microflier combined the cavities with tiny blades, which spun at speeds of up to 13,000 revolutions per minute, to generate
stable, helicopter-like aerodynamic lift. Because the devices rely on hollow cavities rather than motors, gears, or magnetic components, they can be made extremely small and lightweight using a variety of 3D-printing methods. “Our concept is compatible with even further miniaturisation, enabling advanced designs that push the boundaries of robotics and aeronautics,” says first author and MICROBS Lab PhD student Junsun Hwang.
ENERGY-EFFICIENT ROBOTS
Elsewhere, Researchers at Seoul National University of Science and Technology have developed 3D-printed porous foot pads for walking robots that reduce battery power consumption by up to 6.2%. The foot pads use triply periodic minimal
ADDITIVE MANUFACTURING
surface (TPMS) metastructures, lightweight porous geometries that compress on impact and spring back during push-off, storing and releasing mechanical energy with each step. Tested on a commercially available quadruped robot, the system delivered power savings between 1.4% and 6.2% across walking speeds from 0.4 to 1.0m/s, while the robot maintained stable locomotion throughout. The TPMS geometry has already found use in airless tires and soft robotic grippers. The researchers say this application could help produce quieter, longer-running quadruped robots for indoor service, inspection, and logistics deployments.
ADVANCING ADAPTIVE MATERIALS
Adaptive materials – engineered substances that automatically alter their physical properties when exposed to external stimuli – are receiving ever-growing attention in the research space. MIT’s ongoing work in this area has yielded two recent notable breakthroughs. The first centres around the development of a 3D printing system that produces objects capable of changing their surface appearance in response to physical interaction, without the need for electronics. Called ShiftLens, the system enables printed objects to display different images or patterns when a user presses, slides or turns part of the object. “With our system, an object can tell you whether you are using it properly, without the need for sensors or any
Chemical bottles 3D printed with ShiftLens. Image via MIT
complicated electronics,” says Yunzi Zhu, MIT graduate student and lead author of the paper. “The interactive display is mechanical, so you can create a self-contained, multistate, interactive device that a user an control very intuitively. Zhu’s team demonstrated ShiftLens through a chemical bottle that turns green and displays a check mark when its cap is tightly secured, then turns red and shows an exclamation mark when it’s loose. Potential applications include industrial piping that could visually flag a damaged connection, or outdoor warning signs that don’t rely on fragile electronic circuits. Another MIT team recently 3D printed a thermal twisting actuator based on the humidity response mechanics of a pine cone. The work extends more than a decade
Energy-efficient quadruped robot locomotion. Image via Seoul National University of Science and Technology
of category-theory research in corresponding author Markus Buehler’s lab, including earlier categorical prototyping that preserved selected molecular-scale mechanics in large 3D printed parts. According to the research team, this pipeline closes the remaining gap from multiscale biological mechanics through an engineered realisation and fabrication specification to an experimentally validated, machine-executable design. Meanwhile, researchers from Pusan National University in South Korea have developed what they claim is the first 3D printable smectic liquid crystal elastomer ink capable of switching molecular alignment during printing, allowing a single printed filament to elongate or contract when heated. The team lists soft robotic actuators and artificial muscles, reconfigurable surfaces for haptic display, and adaptive textures that regulate aerodynamic drag as realworld applications. And elsewhere, a Heidelberg University team has designed a lightcurable 3D printing polymer that a chemical trigger can take apart at room temperature. As such, printed parts can be broken down into their molecular building blocks in seconds, and then recovered and printed again with the same composition and mechanical properties. The team is targeting vat photopolymerisation methods such as digital light processing that turn liquid inks into fine, light-cured parts for personalised medicine and soft robotics.
www.engineerlive.com
15
INSTRUMENTATION & ELECTRONICS
Avnet Silica estimate based on industry data – July 2026. Source: Avnet Silica Trendliner Q3 2026 report
SEMICONDUCTOR SUPPLY Avnet Silica’s latest Trendliner report indicates a stronger market outlook for semiconductors than earlier in the year, with AI creating both opportunities and constraints
A
vnet Silica’s Trendliner report for the third quarter of 2026 values the semiconductor market at $454 billion, with further growth of 10.8% projected for 2027. This points to a stronger market outlook than earlier in the year, with semiconductor demand strengthening. As indicated by the report, however, supply conditions still remain uneven, with AI infrastructure driving much of the expansion while creating significant pressure on supply chains. “The stronger market outlook is encouraging, but it should not be mistaken for a return to simple or predictable supply conditions,” says Thomas Foj, vice president supplier management, solutions and digitalisation EMEA at Avnet Silica. “AI investment is supporting demand well beyond data centres, while the prioritisation of HBM and other highvalue products is placing pressure
16
www.engineerlive.com
on memory and wider component availability. For industrial customers, early visibility, realistic forecasting, and long-term planning is essential to securing supply.”
EUROPEAN MANUFACTURING IMPROVES
According to the Trendliner report, European manufacturing had its strongest quarter since 2022 during Q2 2026. Eurozone Manufacturing PMI remained above the 50 threshold for a fifth consecutive month, although it eased slightly from 51.6 to 51.4 in June. Manufacturing output increased to 51.7, with new orders also increasing modestly. Export demand remains weak, however, and the International Monetary Fund (IMF) has reduced its 2026 European Union growth forecast from 1.1% to 0.9%. Automotive accounts for 39% of EMEA’s 2026 served semiconductor
market, excluding DRAM, Flash, MPU compute, GPU and AI processors. Industrial electronics represents another 27%. That makes automotive by far the largest semiconductor-consuming vertical in the region. In particular, automotive high-performance computing (HPC) is growing at 21.5% CAGR. This points to increasing semiconductor content associated with software-defined vehicles, ADAS, automated driving and increasingly compute-intensive vehicle architectures.
AI DRIVES DEMAND AND PRESSURE
The report indicates that AI infrastructure continues to underpin sector growth in areas such as memory, high-bandwidth memory (HMB), advanced compute, power management, high-speed interconnect and thermal management. However, this is creating a significant supply side effect. Avnet Silica says
INSTRUMENTATION & ELECTRONICS
EMEA served semi vertical market growth ($B). Source: Avnet Silica Trendliner Q3 2026 report
prioritisation of HBM production is tightening supply across other memory categories, creating cost pressure for PCs, smartphones, servers and other electronics. The report also highlights Edge AI as an increasingly important growth driver, extending AI-related semiconductor demand into industrial and embedded systems and boosting demand for analogue devices, sensors, MCUs and power-management components.
RECOVERY ISN’T LINEAR
Although Avnet Silica describes the market as entering a broadbased recovery, growth remains concentrated in AI infrastructure, memory and advanced compute, rather than representing a completely normalised recovery across all electronics markets. The report cites memory availability
and pricing as the biggest supply chain concern at present. DRAM prices continues to rise because of AI demand and declining DDR4 production. NAND and eMMC prices are also on the rise, with lead times extending beyond 30 weeks for highdensity and automotive products. Price increases are also being felt across NOR and SSD, with tighter availability for PCIe Gen5 and industrial SSDs. MCUs and programmable logic are also under pressure, with 26+ week lead times across 8-bit, 16-bit and 32-bit-and-higher devices. Within programmable logic, Avnet Silica says many parts have lead times of over a year and recommends customers provide visibility through the end of 2027. Alongside memory availability, the report identifies advanced packaging, semiconductor testing and wafer-fab capacity as areas to watch, because AI
According to the Trendliner report, European manufacturing had its strongest quarter since 2022 during Q2 2026
hardware is becoming more complex faster than traditional capacity expansion cycles can accommodate.
THE IMPACT OF GEOPOLITICS
The report argues that tariffs, export controls and localisation requirements are moving from temporary disruptions towards long-term considerations. Diversification is improving resilience, but it also introduces additional complexity and cost. Regionalisation therefore helps reduce risk but isn’t a quick solution to capacity constraints – particularly for memory. Asia continues to lead the market’s growth, supported by sustained investment and accelerated technology adoption across multiple sectors. In essence, the report shows that while the industry is no longer facing the same broad-based shortages seen earlier in the decade, shortages and price pressure are becoming more selective, concentrated around AIdriven demand, memory, certain MCUs, sensors, programmable logic and automotive and industrial components. The coming months will show whether recent order strength across Europe, in particular, can translate into a broader recovery for the semiconductor market as a whole.
www.engineerlive.com
17
INSTRUMENTATION & ELECTRONICS
Coming Soon
HIGHER VISCOSITY JETTING On a proven platform that Just keeps getting better
PROFESSIONAL 1AC & 3AC DIN RAIL POWER SUPPLY SOLUTIONS, REDUNDANCY DIODES & E-FUSES The New RACPRO1 Series from 120-960W
re c o m - p ow e r. c o m / ra c p ro
SINCE 1975, WE POWER YOUR PRODUCTS
18
www.engineerlive.com
INSTRUMENTATION & ELECTRONICS
Within GoPxL, imported AI models can operate alongside traditional rules-based tools in the same inspection pipeline
UNLOCKING EDGE AI
A
LMI Technologies’ Annika Meininger discusses the engineering case for open architecture
rtificial intelligence (AI) is becoming an increasingly important component of industrial machine vision. As AI moves into production inspection, vision engineers face a fundamental architecture decision: how tightly should AI model
development be coupled to the hardware and software responsible for executing the inspection? Closed vision ecosystems can simplify initial deployment but may restrict engineers to vendorspecific development tools and workflows. Custom PC architectures
provide greater flexibility but can introduce significant integration requirements across cameras, GPUs, inference engines, vision libraries, communications, and visualisation. The challenge is that these technologies operate on different lifecycles. Industrial vision hardware
AI and rule-based vision
www.engineerlive.com
19
INSTRUMENTATION & ELECTRONICS
may remain in production for years, while AI frameworks, model architectures, and training environments evolve much more rapidly. A flexible architecture therefore needs to separate AI model development from production execution.
A flexible architecture needs to separate AI model development from production execution
DECOUPLING DEVELOPMENT FROM EXECUTION
Bring Your Own Model (BYOM), introduced in GoPxL 1.6, applies this principle across 2D and 3D inspection applications. Engineers can import compatible YOLO models developed outside the GoPxL training environment, including Ultralytics models such as YOLO 26. Models can be developed using Roboflow or other preferred AI frameworks and training infrastructure, allowing engineering teams to retain control over data preparation, labelling, training, and model selection. Once trained, imported models can be incorporated directly into a GoPxL inspection pipeline alongside traditional vision tools. This creates an important architectural distinction: the production vision environment can execute the model without dictating how that model is developed.
AI can address complex classification or visual variation, while deterministic tools handle geometric measurement, tolerances, and decision logic
FLEXIBLE EDGE DEPLOYMENT FOR 2D AND 3D
GoPxL extends this flexibility to deployment. Imported models can run on PC or GoMax acceleration without requiring a GoPxL Pro Tools runtime license, using open-source inference tools that can also be customised for application-specific requirements. For 2D applications, the Image Inference Tool executes imported models on image data, including directly on supported Gocator 2D Smart Cameras. For 3D applications, the Surface Inference Tool applies imported models to surface data using PC or GoMax compute. Surface inference is not executed onboard Gocator 3D sensors. This provides a common approach to BYOM across both 2D and 3D inspection while allowing compute resources to be selected according to application requirements.
20
www.engineerlive.com
INTEGRATING AI INTO THE INSPECTION PIPELINE
A production vision system must do more than execute inference. It must acquire and pre-process data, perform measurements, generate decisions, communicate with factory equipment, and provide visualisation and diagnostics. Within GoPxL, imported AI models can operate alongside traditional rules-based tools in the same inspection pipeline. AI can address complex classification or visual variation, while deterministic tools handle geometric measurement, tolerances, and decision logic. The engineering value of open edge
AI is therefore not simply greater model choice. It is the ability to develop models using the tools best suited to the application, deploy them across a scalable industrial vision architecture, and integrate AI with established machine vision workflows without building a custom software stack around every inspection. As AI technologies continue to evolve, this separation helps keep the production architecture stable while allowing the AI layer to advance independently.
Annika Meininger is at LMI Technologies: www.lmi3d.com
INSTRUMENTATION & ELECTRONICS
YOUR DESIGN - YOUR CHOICE From DC/DC Low Power ICs (1-30W) to Ready-Made Discrete Solutions
SPEED UP YOUR TTM
SOLUTION PROVIDER
FOR ALL POWER APPLICATIONS
w w w. r e c o m - p o w e r. c o m / i c
ASC INERTIAL SENSORS
Accurate. Precise. Certified.
asc-sensors.de
Unlocking superior railway performance Accurate: ASC sensors produce results that are very close to the actual value Precise: ASC sensors remain very consistent across repeated measurements ■ Certified: The ASC RAIL series are certified to applicable norms including EN 50155, EN 50121-3-2 and EN 45545. They provide reliable solutions that meet national and international standards ■ Reliable: Robust to prevail extreme testing and operational conditions ■ ■
Worldwide, railway manufacturers and operators rely on tailor-made solutions from ASC. When may we have the opportunity to convince you?
ASC inertial sensors are used for Characterization of track geometry (EN 13848) Specifying structural requirements for bogie frames (EN 13749) Dynamic interaction between pantograph and overhead contact line (EN 50317) Passenger ride comfort (EN 12299) Running characteristics of railway vehicles (EN 14363)
Gyroscopes
MEMS accelerometers
ASC_Anzeige_Rail_IME_185x121_02.indd 1
IMUs
Smart sensor systems
SUCCESSFUL WORLDWIDE. AT HOME IN GERM ANY.
13.04.26 17:49
www.engineerlive.com
21
INSTRUMENTATION & ELECTRONICS
Smart Industrial 2D Vision with Deep Edge AI Gocator® 2D cameras combine high-speed imaging and deep edge AI (deep learning–powered intelligence executed on the device itself) in a compact, IP67–rated package. Built on the NVIDIA Jetson Orin NX, these cameras are powered by onboard GoPxL IIoT vision software. These cameras capture, inspect, and output results at up to 84 fps without the need for a PC, cloud, or middleware. They provide powerful inspection performance straight from the camera.
Learn More
Engineering magazines
FREE subscription
Available online, on your tablet or on your mobile October 2026 SUBSCRIBE FOR FREE
April 2026
www.engineerlive.com
SUBSCRIBE FOR FREE
.com www.engineerlive
MICRO MACHINES
July 2026 SUBSCRIBE FOR FREE
BREAK
www.engineerlive .com
G RECORIN DS A 0.2% moto r efficiency gain could billion-dollar deliver savings for global indus try
A NEW
N
DIRECTIO
of in the era Steer-by-wire efined vehicle the software-d
ON THE EDGE LIFE LARGER THAN is enabling LFAM ons How robotic te applicati new composi
industrial edge AI in cs The role of r-grade electroni and consume
Micro-precision 3D printing is offering game-changing design freedom in electronics
CONTROLLED LIFTING
DESIGNING FOR RELIABILITY
Why motor control is key for optimising ESP installations
Integrating sustainability into EV manufacturing processes
THE ALLOY ADVANTAGE
Reducing vehicle cost and weight complexity, with AHSS
SELF-HEALING SPACECRAFT
Composites could reusable spacraft transform design
www.engineerlive.com 22
www.engineerlive.com
INSTRUMENTATION & ELECTRONICS
COUPLING QUBITS MIT’s new qubit architecture is enabling faster, more accurate quantum computing operations
R
esearchers at MIT have developed a superconducting qubit architecture designed to address one of the key engineering challenges facing scalable quantum computing: achieving both long coherence times and rapid, reliable interactions with the rest of a quantum system. The architecture, described as an “arm qubit”, separates these functions into two connected components. A dedicated data mode stores quantum information, while an arm mode provides the strong interactions needed to communicate with other qubits and electronic components. Simulations indicate that the approach can deliver faster operations and readout while maintaining state-ofthe-art coherence.
Kevin O’Brien, associate professor in electrical engineering and computer science (EECS) at MIT. The new architecture tackles the competing requirements by assigning different tasks to separate modes. The data mode uses a qubit design known for its long coherence, while the arm mode is based on a design capable of strong interactions with components including resonators used to read out quantum states. “It is engineered for these two, dual purposes – accomplished together by the data mode and arm mode – and these two goals really matter when you try to do quantum error correction,” adds Alec Yen, an EECS PhD graduate and co-author of the research.
A CRITICAL COMBINATION
A key element of the architecture is a specialised coupling device previously developed by the MIT researchers. Known as a quarton coupler, it provides strong nonlinear coupling between the data and arm modes while limiting unwanted mixing. Nonlinear coupling is important because it enables changes in one quantum component to influence another, forming a basis for many quantum operations. Conventional approaches, however, can introduce unwanted interactions that become increasingly problematic as systems scale. “By dedicating the ‘arm’ component to coupling, we were able make a design that is scalable, robust to
Unlike classical bits, qubits are highly susceptible to decoherence, which causes stored quantum information to degrade and introduces errors into calculations. As more qubits are interconnected, unwanted interactions can compound the problem, limiting the length and complexity of algorithms that can be executed reliably. “The goal for doing all this is to build a fault-tolerant quantum computer where you can correct these errors as they happen, so then you can do long computations and actually do useful things with a quantum computer,” explains
CONTROLLING NONLINEAR COUPLING
manufacturing errors, and still uses a quarton coupler to achieve strong nonlinear coupling,” explains Jeremy Kline, an EECS graduate student and lead author of the study. Simulation results showed the arm qubit outperforming other superconducting qubit architectures, combining long coherence with faster operations and readout. These characteristics could be particularly valuable for quantum error correction, where computational speed and qubit fidelity directly influence how effectively errors can be detected and corrected before they propagate. The researchers emphasise that the work remains at an early stage. The next step is to fabricate the architecture and experimentally determine whether its simulated performance translates into a physical device. “This work leaves me with a lot of suspense because our simulations are very promising. Next, we’ll need to see if we can make it, and determine whether we missed anything in the modelling or design. If we can fabricate this qubit, it could be a building block for future errorcorrecting quantum computers,” O’Brien says. The research is published in Physical Review Applied and was supported in part by the Army Research Office, Air Force Office of Scientific Research, MIT Centre for Quantum Engineering and Laboratory for Physical Sciences.
www.engineerlive.com
23
INSTRUMENTATION & ELECTRONICS
Intelligent power ICs provide an additional level of architectural flexibility
RETHINKING
POWER DESIGN Stanislav Suchovsky explains how integrated power ICs create new options between pre-qualified modules and fully discrete power architectures
I
solated DC/DC conversion has traditionally presented design teams with a straightforward choice: use a pre-qualified module to minimise development risk, or build the power stage from discrete components to gain greater control over cost, layout and electrical performance. That distinction is becoming less clear. A new generation of highly integrated transformer-driver, flyback-controller and synchronous-rectifier ICs allows engineers to retain many of the practical advantages of a module
24
www.engineerlive.com
while gaining more freedom over the final power architecture. This matters because isolation requirements are becoming more varied. Industrial automation, sensing, communications and widebandgap semiconductor (WBG) gate driver power supplies may require non-standard voltages, multiple isolated outputs, asymmetric rails or unusual mechanical constraints. A fixed module remains attractive when the electrical specification is conventional and time-to-market (TTM) is the main priority. When the
power stage has to fit the application rather than the other way around, however, an integrated circuit (IC)based approach can provide greater system-level flexibility.
WHY THE BUILD VERSUS BUY EQUATION IS CHANGING One important enabler is integration at semiconductor level. Instead of implementing switching, timing, protection and rectification with numerous discrete devices, designers can use power ICs that combine
INSTRUMENTATION & ELECTRONICS
can address multiple outputs, asymmetric gate-drive rails or specific creepage and clearance distances.
FROM PROTOTYPE TO PRODUCTION
Recom offers modular and discrete DC/DC power modules
several of these functions in compact packages. Recom, for example, offers push-pull transformer drivers, fullbridge transformer drivers, regulated flyback controllers and synchronous rectifier controllers that support discrete isolated power architectures. On the primary side, intelligent transformer drivers generate the alternating waveform required by the isolation transformer and can integrate protection and switchingcontrol functions. Adaptive dead-time control is particularly important. In push-pull and full-bridge circuits, unwanted switch overlap can cause shoot-through, while switching asymmetry can contribute to magnetic flux imbalance and core saturation. Precisely controlled dead time reduces these risks and helps maintain predictable operation as temperature, load and component characteristics change. Topology still matters. A pushpull converter is well suited to low-voltage, higher-current systems. It uses a centre-tapped primary winding and alternates current through the two halves of the transformer. A full-bridge topology energises the complete primary winding and does not require a centre tap, making it attractive where higher input voltages and lower currents dominate. For applications that need a wide input voltage range, tighter regulation or higher power, a flyback controller adds closed-loop pulsewidth modulation (PWM) regulation. Recom’s RVPW series supports regulated flyback designs up to 30W.
EFFICIENCY DOESN’T END AT THE TRANSFORMER
The secondary side is equally important. Conventional rectifier diodes are simple and robust, but their forward voltage drop becomes increasingly significant as output voltage falls or current rises. Synchronous rectification replaces the diode conduction path with metal-oxide-semiconductor fieldeffect transistor “MOSFET switches”, reducing conduction losses and the associated thermal load. Smart rectifier and synchronous rectifier controller ICs can also simplify secondary-side control. Recom’s RVS and RVSY families use self-synchronising concepts that reduce the need for separate control signals from the primary side. This can simplify the implementation of compact isolated converters while improving efficiency compared with conventional diode rectification. The transformer remains a central part of the architecture. Its turns ratio establishes the relationship between input and output voltages, while winding construction influences isolation, leakage inductance, isolation capacitance and available printed circuit board (PCB) space. Standard surface-mount device (SMD) transformers cover many common requirements, while custom magnetics
The strongest argument for an integrated power module is still development speed. A pre-qualified module arrives as a known electrical and mechanical building block, reducing schematic work, layout iteration and qualification effort. At lower volumes, it can also simplify the bill of materials (BOM), supplier qualification and assembly planning by consolidating the isolated supply into a defined component. An IC-based solution requires more engineering, particularly in magnetics, electromagnetic compatibility (EMC), thermal design and PCB layout. Critical current loops should be short, the driver and transformer should be placed close together, and input and output capacitors should be positioned to minimise parasitic inductance and output ripple voltage. The economic balance can change with production volume. Recom’s internal total-cost analysis indicates a typical crossover point at around 50,000 units per year, although the actual threshold depends on assembly processes, component sharing, qualification effort and engineering resources. Above that level, a discrete architecture may become more attractive because the transformer, silicon and passive components can be optimised for the exact application. The wider significance is that the choice between an integrated power module and discrete components is no longer necessarily an all-ornothing decision. Engineers can prototype with a module, move to validated component sets of ICs and transformers as requirements stabilise, and adopt a more customised power stage for high-volume production. Intelligent power ICs therefore provide another level of architectural flexibility, allowing design teams to select the degree of integration that best matches each stage of the product lifecycle.
Stanislav Suchovsky MSc is technology engineer at Recom Power: www.recom-power.com/ic
www.engineerlive.com
25
MATERIALS, PROCESSES & FINISHES
SELF-HEALING
VEHICLES
Scratches, scuffs and punctures are facts of life for most drivers. But a new generation of self-healing materials could make everyday damage less of a problem, says Alex Harvey – senior associate and patent attorney at Withers & Rogers
Alex Harvey, senior associate and patent attorney at Withers & Rogers
C
armakers are already using self-healing materials in coatings, protective films and tyres. But how well do they work, and could they be used more widely in the future? Self-healing paintwork is already appearing on some high-end models. These smart coatings are designed to deal with light damage, such as swirl marks from washing or minor scratches picked up in day-to-day use. Hyundai, for example, has recently filed a US patent application directed to a self-healing polyurethane coating film, and manufacturers such as Toyota and BMW have explored similar approaches. The basic idea is straightforward; the coatings often contain shape-
26
www.engineerlive.com
memory polymers that react to warmth from sunlight or hot water. As the material heats up, the polymer chains relax and become more mobile, which causes them to naturally return to their original form, thereby erasing any light scratches. These smart coatings are often described as having “intrinsic” self-healing properties, as they are built into the material itself. Tyres take a slightly different, extrinsic approach. Notably, many self-healing tyres use a layer of sealant embedded inside the tread. If a nail or screw pierces the tyre, the sealant flows into the hole and forms an airtight plug. Whilst it won’t make the tyre as good as new, this repair can keep air loss under control long enough for the driver to reach a garage safely.
MATERIALS, PROCESSES & FINISHES
A car that can shrug off minor scratches, keep its finish looking fresher for longer, or buy extra time after a puncture could be cheaper and less stressful to live with
Self-healing polyurethane coatings are gaining traction amongst car manufacturers
THE APPEAL IS NOT JUST AESTHETIC
A car that can shrug off minor scratches, keep its finish looking fresher for longer, or buy extra time after a puncture could be cheaper and less stressful to live with. For now, these materials are mainly about convenience, appearance and dealing with small-scale damage rather than fixing serious faults. However, the technology underpinning many self-healing materials can also find use in safetycritical applications, particularly in the aerospace industry, where the ability to carry out in-flight repairs to aircraft and satellites can offer a vital safety net. One eye-catching example developed by NASA in 2015 is a
multi-layer ballistic polymer designed to help protect spacecraft from high-speed ballistic debris. The concept works in a similar way to a self-healing tyre. A viscous liquid monomer is sandwiched between a pair of solid polymer panels, ready to react when damage occurs. If a fast-moving projectile punctures the outer layer of the polymer, the liquid monomer flows into the breach and quickly solidifies upon contact with oxygen, plugging the hole before the damage can spread. Another approach uses microscopic capsules hidden inside the material itself. For example, MPB Communications has been granted patent protection in the US (US8865798B2) for a self-healing composite for outer-space structures, in which the material matrix contains tiny capsules filled with a liquid healing agent. When a crack forms, the capsules rupture and release the healing agent into the damaged area, where it bonds with the surrounding matrix and helps repair the crack. In effect, the material carries its own first-aid kit. European researchers are pushing the idea further with a smart composite called HealTech. Rather than simply reacting after damage occurs, the material is designed to sense cracks and then trigger a targeted repair using heat. Developed as part of the European Space Agency’s Project Cassandra, HealTech utilises a specialised carbon-fibre
reinforced polymer with embedded internal sensors and 3D-printed aluminium heating grids. When damage is detected, the heating grids locally heat the affected area, which activates a healing agent provided inside the composite which can repair cracks or micro-fractures. Projects such as this provide a glimpse of a future in which critical structures can monitor their own health and carry out targeted repairs on damaged areas.
BRIGHT FUTURE
Whilst much R&D activity is at an early stage, it is evident that selfhealing materials could find many different uses in the future. The intrinsic nature of many self-healing materials makes them ideally suited to autonomous cars, where they could be used to protect sensors and cameras from visual obstruction, ensuring safe and reliable operation. Self-healing composites could also be used to extend the life of damageprone wind turbines. With so much innovation activity underway and so much still to learn about the capabilities of self-healing materials, it’s recommended for innovators to seek advice about intellectual property (IP) protection at an early stage. Research-led initiatives often involve some degree of collaboration, and it is just as important to ensure pre-existing IP is protected, as it is to secure a stake in any new IP created together.
www.engineerlive.com
27
MATERIALS, PROCESSES, FINISHES
Parylene Medical and Electronics Coating Ultra thin bio compatible protection Outstanding chemical, moisture and electrical barrier protection High lubricious dry film conformal coating Metals, Elastomers, Electronics and Plastic Proprietary Dimer is 99.7% pure CW Parylene: USP Class VI and ISO10993 tested MAF No. 1176 on file with the FDA
www.cwst.com | +353 (91) 780 300 Curtiss-Wright, Surface Technologies Division, Parkmore Business Campus, Parkmore West, Galway, Ireland
ENGINEERING CLEAN AIR. Your complete LEV partner Design | Installation | Commissioning | Servicing | LEV TExT
01604 635333 www.mccarthy-environmental.co.uk
28
www.engineerlive.com
MATERIALS, PROCESSES & FINISHES
Temperature, humidity and dew point can all affect the application and curing of a coating
COATING CONDITIONS
W
hen a protective coating does not perform as expected, the coating itself is often the first thing to come under scrutiny. But premature deterioration is rarely down to one thing. The performance of a coating system can be affected by decisions made before application starts, the condition of the substrate, the environment during the work and the checks carried out along the way. What happens after the project is complete, matters too. Established corrosion protection
Director of Paint Inspection Ian Patterson explains why assessing coating performance begins long before the first coat is applied
guidance, including the ISO 12944 series, takes this wider view. It covers factors such as the environment, surface preparation, coating systems, application and maintenance rather than treating the coating as an isolated product. For asset owners, contractors and specifiers, that is an important distinction. A coating can be well suited to the job and still fail to deliver the expected service life if the conditions around it are not right.
SPECIFICATION SHOULD REFLECT THE ASSET Coating selection should therefore
start with the environment in which the asset will operate. Steel inside a relatively dry building faces a very different level of corrosion risk from infrastructure exposed to coastal weather, industrial pollutants, persistent moisture or immersion. Even within one structure, different areas can be exposed to diverse conditions. The expected service life also matters. An accessible structure may be straightforward to inspect and maintain regularly, whereas a coating applied to a difficult-to-reach or costly-to-access asset may need to perform for much longer before major
www.engineerlive.com
29
MATERIALS, PROCESSES & FINISHES
maintenance can be carried out. This is why specification should be based on the asset and its environment rather than simply choosing a familiar coating product. ISO 12944-2, for example, classifies different exposure environments because the level and type of corrosion stress is an important part of selecting a suitable protective system.
SURFACE PREPARATION
Surface preparation can sometimes be treated as a job that needs to be finished before the “real” work begins. In practice, it has a direct bearing on how the coating performs afterwards. The coating has to adhere to the surface it is being applied to. Rust, mill scale, grease, soluble salts and poorly prepared existing coatings can all interfere with adhesion or contribute to problems beneath a new system. Surface profile also needs to be appropriate for the coating being used. The surface needs enough profile to support adhesion, without creating peaks that are difficult to cover properly. There is no universal preparation method that suits every project. The appropriate standard depends on the substrate, the existing condition, the coating system and the environment. ISO 12944-4 sets out surface preparation grades for different types of steel surfaces, reinforcing the importance of treating preparation as part of the specification rather than an afterthought. Two projects can use the same coating and still produce very different results if the surfaces underneath have been prepared differently.
APPLICATION CONDITIONS
Temperature, humidity and dew point can all affect the application and curing of a coating. If the steel temperature is too close to the dew point, condensation can form on the surface. That may not always be obvious to the person applying the coating, but moisture at the wrong stage can affect the finished system. Film thickness matters too. Applying too little material can leave the substrate inadequately protected, while applying more than specified is not automatically better.
30
www.engineerlive.com
Depending on the product, excessive film thickness can introduce its own problems. Mixing, application methods and recoating intervals also need to follow the coating manufacturer’s requirements. The coating needs to be applied in the conditions and at the thickness for which the system was designed.
THE IMPORTANCE OF INSPECTION
Inspection during surface preparation can establish whether the required level of cleanliness and surface profile has been achieved before the surface is coated. Environmental conditions can then be monitored during application, while dry film thickness measurements can confirm whether the specified coating build has been achieved. This is where independent inspection can be particularly valuable. It creates a record of what actually happened during the work, rather than relying on assumptions once the finished coating is in place. It also means problems can be picked up when they are still possible to address. Finding an unsuitable surface before coating is applied is very different from discovering a failure several years later.
COATING FAILURES
When a coating begins to deteriorate, it is tempting to blame the product. The appearance of the failure alone, however, does not necessarily tell you what caused it. Loss of adhesion may be associated with contamination, surface preparation or moisture. Localised corrosion may develop where the coating has been damaged or where the required film thickness has not been achieved. Problems between coats can also be linked to application conditions or recoating intervals. A proper failure investigation therefore needs to look beyond the coating itself. Records of the original surface condition, preparation, environmental readings, coating thickness and application process can be extremely useful when trying to establish what happened. Without them, the cause can be much harder to determine.
MAINTENANCE MATTERS A protective coating is intended to extend the working life of an asset. It does not remove the need for inspection and maintenance. Coatings can suffer wear, impact damage and localised corrosion even when the wider system remains in reasonable condition. Regular inspections can help identify these areas before a relatively small repair develops into a much larger project. Future maintenance should therefore be considered when the coating system is first specified. Access, inspection requirements and the practicalities of carrying out repairs can all influence which system is most appropriate. Ultimately, coating performance comes down to the whole process rather than one stage in isolation. The specification determines what the system needs to achieve. Preparation provides the surface it needs to adhere to. Application conditions affect how it cures and builds. Inspection provides evidence that the work has been carried out correctly, while maintenance helps protect the asset once it is back in service. The coating itself remains important, but it is only one part of the equation. Looking at the full lifecycle gives asset owners and contractors a much better chance of achieving the level of protection and durability they expected when the system was specified.
Plastic Coatings
Coating solutions for electric vehicle technologies • Approved applicators of Resicoat, PPA, Nylon, Halar, Plastisol PVC, 3M Skotchkote • Electrical insulation up to 30Kv
t: 0800 0086903
• Smaller batches or Mass production • IATF 16949 approved supplier Already nominated on several new vehicles • Supplier of Aerospace Busbar coatings for over 20 years
...the experts in finishing • ISO 9001 • IATF 16949 • ISO 14001 • OHSAS 18001
www.plasticcoatings.co.uk e: enquiries@plastic-coatings.com
MATERIALS, PROCESSES & FINISHES Having a broad range of coating capabilities under one roof allows the company to handle a wide variety of requirements and industries
The company’s 24-hour processing facility in Kingswinford
A SPECIALIST FINISH Lydia Arundel hears how Plastic Coatings has transitioned from specialist finishing to long-term manufacturing partnerships
P
lastic Coatings has spent decades developing its expertise in industrial coating and finishing, working across sectors such as automotive, oil and gas, aerospace and defence. Its history reflects many of the changes that have shaped UK manufacturing, from tighter legislation and rising costs to changing supply chains and increasing demands on specialist processes. During International Design Engineer’s visit to the company’s 24-hour processing facility in Kingswinford, the West Midlands, I spoke to Carl Allison, Director of Plastic Coatings, about the evolution of the business, the challenges of running a specialist finishing operation, investment in plant and equipment, and why manufacturers continue to rely on specialist subcontractors.
TELL US ABOUT YOUR BACKGROUND AND WHAT LED YOU TO YOUR CURRENT POSITION?
I started in engineering around 25 years ago with a Japanese company at a greenfield UK site, manufacturing water pumps and oil pumps for the automotive industry. I then moved to
32
www.engineerlive.com
a more traditional UK engineering company specialising in tube manipulation, with some aerospace work but primarily automotive. I joined Plastic Coatings from there, initially working in quality engineering, which was my discipline at the time. About 12 years ago, I moved over to the commercial side, bringing more of an engineer-led approach to selling. That means solution-based selling rather than simply saying we have a great range of products, or we can be cheaper than everyone else. It’s about finding a solution that works for the customer.
WHAT ARE THE BIGGEST CHALLENGES AND OPPORTUNITIES FOR THE BUSINESS CURRENTLY?
The biggest challenge right now is unpredictability. You just don’t know what’s going to happen from one day to the next. At the moment, we have around 48–72 hours of workload ahead of us, but there’s no guarantee after that. I know I’ve got two days’ work for the 80 people we have working here. If nothing comes in tomorrow, on day three I’ve got nothing for the day after.
The biggest opportunity is the significant increase in spending on defence. Our turnover in defence is around five times what it was in the prior year, and we expect that to continue increasing. Nuclear is another good opportunity, with a lot of money being spent in the UK on nuclear infrastructure.
WHICH MARKETS ARE MOST IMPORTANT TO YOU?
Our biggest single industry is oil and gas. Probably 30–35% of our turnover is in oil and gas, split between the fastener business, filter screens and some ancillary products, including valves and bits of pipework.
HOW HAS THE FINISHING INDUSTRY CHANGED IN THE LAST 20 YEARS?
The biggest change is probably the reduction in the number of competitors. There used to be finishing companies everywhere, but changes in legislation, costs and environmental requirements have pushed costs up and driven people out of the market. That has got rid of a lot of the competition, but it has also got rid of a
MATERIALS, PROCESSES & FINISHES Plastic Coatings has spent decades developing its expertise in industrial coating and finishing
lot of the market. There isn’t as much manufacturing in the UK anymore compared with where we were 20 years ago.
WHAT ARE THE BIGGEST CHALLENGES YOU SEE AHEAD?
The biggest thing we’re preparing for is the change in the energy market. Most of our processes run on gas, and electricity is seven or eight times the price of gas. We’re looking at sustainability measures such as solar power and green sourcing of energy, and we’ve got a zero-carbon roadmap. I think that’s going to be the biggest challenge over the next 10–15 years as the Government drives further towards net zero and energy-intensive industries like ours look to remain competitive. There are significant subsidies abroad that we don’t get in the UK. If your cost base is moved significantly by energy prices, minimum wage and everything else, you can’t compete. Brexit also means that everything you try to get out of the country carries some sort of tariff or levy, and anything you try to bring in has the same. It’s very difficult to compete with that.
WHEN DID PLASTIC COATINGS MOVE TO THIS SITE?
Plastic Coatings started in 1952 in Guildford, operating with a small team of people dipping metal into plastic to provide corrosion-resistant coatings. The business outgrew that site and moved here sometime in the 1960s. At one point we had five or six sites
around the country, but over time we consolidated back to one site here.
HOW IMPORTANT IS HAVING SUCH A BROAD RANGE OF COATING CAPABILITIES UNDER ONE ROOF?
We’re one of a very limited number of companies in the UK with the range of coatings we have. Having that capability under one roof means we can handle a wide variety of requirements and work for different industries, rather than being reliant on one particular market.
Plastic coatings’ biggest single market is oil and gas
how to keep them running.
HAS GROWTH IN DEFENCE SPENDING CHANGED THE TYPE OF WORK YOU’RE TAKING ON?
Defence has always been a specialist market, but with increased spending and increased volumes, specialist capacity is being used up. Defence manufacturers are therefore looking to other manufacturers to do work they might not previously have outsourced. We’ve done PVC coating for BAE Systems for more than 40 years, but we’d never done wet paints such as Desert Tan and NATO Green. We’ve been doing a lot of that work over the last six months.
HOW MUCH INVESTMENT IS REQUIRED TO MAINTAIN THE PLANT, AND IS MAINTENANCE A SIGNIFICANT LOOKING AHEAD CHALLENGE? From maintaining a wide range of I’d say about £4.5 million to set up all the equipment, and probably £1.5 million has been spent over the last 10 years updating it. We don’t replace the whole plant every time technology changes; we replace individual parts. That might mean updating a spray booth or adding automation to a spray booth, rather than replacing the whole electrostatic oven, track and everything else. Maintenance is a big deal for us. Finding people who understand the plant and equipment is difficult because it’s quite different from a normal industrial plant. We’ve got things like conveyors, but the ovens are a very niche piece of equipment and you need people who understand
processes and equipment to managing changing customer requirements, energy costs and recruitment, the challenges extend well beyond the coating process itself. For Plastic Coatings, much of that capability has been built over decades through investment, experience and the retention of specialist knowledge. As the business continues to respond to changing markets and manufacturing requirements, that combination of technical expertise, flexibility and people remains central to its operation.
For more information visit: www.plasticcoatings.co.uk
www.engineerlive.com
33
LIGHTEN UP
COMPOSITES
RE-CELL is developing supercapacitors and structural batteries based on recycled carbon fibre
A PARADIGM SHIFT How Aimplas’ IN AERONAUTICAL ongoing projects are COMPONENT DESIGN Aimplas’ RE-CELL project is helping aeronautics a novel generation of and transport vehicle developing supercapacitors and structural manufacturers reduce batteries based on recycled carbon fibre, capable of storing energy while weight and improve simultaneously forming part of the energy efficiency aircraft structure itself. The initiative
W
ith over three decades of experience in the plastics industry, Aimplas is a technology partner to hundreds of companies, from raw material manufacturers through to plastic processors and end users. As such, the company’s R&D arm is extensive, with 307 projects either completed or ongoing. Two of these projects are currently addressing the major challenges facing the aeronautics and vehicle manufacturing industries: weight reduction and energy efficiency. As these sectors transition to more sustainable technologies – in light of global emissions targets and decarbonisation – innovative composite technologies and materials are gaining increasing traction.
34
www.engineerlive.com
is coordinated by Sofitec with participation from Aimplas, the Plastics Technology Centre and I2CON. The project is using multifunctional materials that combine mechanical properties with energy-storage capacity to design lighter, more energy efficient aeronautical components. “The major challenge in aviation electrification is not only to store more energy, but to do so without adding a weight penalty,” says Esteban Castro, R&D engineer at Sofitec. “Structural batteries make precisely that possible: the component itself performs both a structural and an energy function.” The project will initially focus on non-critical applications such as cabin lighting systems, with broader integration planned in future. Recycled carbon fibre will be used as the basis for developing these new
materials, which the partners say will not only help to reduce waste in composite-intensive sectors but also support progress towards a circular economy model. “In RE-CELL, we are not only seeking more efficient new materials, but also more sustainable ones,” adds Fernando Ramos, researcher in sustainable and future mobility at Aimplas. “We are working to give carbon fibre a second life and turn it into a high-value resource for demanding applications such as aeronautics.” The project is also addressing some of the scientific challenges that have so far limited the real-world application of structural batteries, such as the development of functional solid electrolytes and the variability of recycled fibres. Florin Ardelean, a researcher in computational modelling and simulation at I2CON, explains: “One of the project’s main advances is to address together phenomena that until now have been studied separately, such as ionic conduction and the material’s mechanical behaviour. This integrated approach is essential to leap to real applications.”
COMPOSITES
Recyclable ultralight panel for structural transport applications
The project will culminate in the manufacture and validation of a fullscale demonstrator integrated into a component linked to an aircraft landing gear. This step will make it possible to assess the technology’s performance under representative conditions and advance towards future industrialisation.
ULTRALIGHT AND RECYCLABLE VEHICLE PANELS
Aimplas is also looking to address lightweighting in the SUPERPAN project, an initiative led by Birka Composites with participation from Ideko, which aims to develop a new generation of multi-directionally reinforced panels for use in structural transport components. With vehicle weight a decisive factor in reducing energy consumption and emissions,
the ultralight panels will have greater recycling potential. “The aim is to advance towards more efficient materials that reduce the weight of structures without compromising safety or performance,” says Manuel Guerrero of Birka. One of the project’s main advances is a focus on materials that are easier to recycle at the end of their useful life. At present, many components used in transport are difficult to recover. SUPERPAN proposes an alternative based on thermoplastic matrices, which improve the recyclability of composite materials and support the development of solutions aligned with circular-economy principles. Materials are designed and selected from a global perspective that considers the component’s entire service life and adapts established manufacturing processes that
Vehicle weight is a decisive factor in reducing energy consumption and emissions
currently use thermosetting resins. The project integrates automated manufacturing technologies such as dual pullbraiding (DPB), a technology patented by Birka, and ultraviolet (UV)-assisted curing of prepregs. These technologies improve process efficiency, reduce costs and decrease the variability associated with manual processes. Controllers are also integrated into the manufacturing line to collect process data. This automation enables products to be manufactured with greater quality control and fewer defects, while increasing productivity and scalability. Aimplas is contributing its expertise in polymer materials, recyclability, material characterisation and validation, as well as supporting the development of advanced manufacturing processes. Ideko, meanwhile, will supply its knowledge of automated manufacturing technologies and industrial digitalisation. Vehicle weight is a decisive factor in reducing energy consumption and emissions. As such, composite materials have become a strategic alternative because they offer high strength and lower weight than traditional materials such as metals.
www.engineerlive.com
35
COMPOSITES
E
NC North Composites Engineering Ltd Training Unique ‘know how’ based courses in Composite Design, Analysis and Manufacture Specialist in Aerospace, Marine, and Automotive sectors
Cleanroom Solutions Design, specification, set up and expansion of composite workshop and cleanroom equipment Design and manufacture of composite curing and repair equipment Ready to expand your horizons Email: info@northcompositesengineering.co.uk www.northcompositesengineering.co.uk
36
www.engineerlive.com
COMPOSITES
COMPOSITES TAKE FLIGHT A recent JEC whitepaper says tomorrow’s air travel will depend on composite materials for fuel efficiency, durability and sustainability
C
omposites have been utilised within commercial aerostructures for decades, though aluminium has remained dominant. Increasingly, though, composite materials are becoming more common in fuselage, wing, tail and other aircraft structures. “Composites have earned a permanent seat at the table in aerospace design,” says Collin Heller, VP at Counterpoint Market Intelligence. “As the industry continues to push the boundary on efficiency, composites have gone from an advantage to a necessity.” In the next five years, Airbus and Boeing are each preparing to launch a clean-sheet, next-generation singleaisle aircraft to replace the A380 and 737 respectively. The timing of JEC’s whitepaper produced in partnership with Counterpoint Intelligence, Composite materials in aeronautics, is therefore timely. “The next-generation of singleaisle aircraft Airbus and Boeing are developing will likely be the most consequential programmes the composite industry will face for the next 25 years,” predicts JEC’s global content advisor and editor, Jeff Sloan. The new aircraft are expected to have composites content on a par with the A350 and the 787. However, where the widebodies are currently being built at rates around 10 aircraft per month, a next-gen single-aisle programme could be produced at a rate of up to 100 per month. Meeting that rate will test the whole composites supply chain. Next-generation wings are almost certain to be composite. A composite fuselage is within reach if the industry can solve certain manufacturing challenges. Flight efficiency, fuel consumption, and
sustainability will all turn on these decisions, the whitepaper says.
KEY FINDINGS
According to the whitepaper, composites now account for more than half of the structure of the latest airliners. The most significant shift has been from aluminium-dominated airframes to composite-intensive designs. The Boeing 787 contains around 50% composites by structural weight, while the Airbus A350 reaches 53%. These aircraft use carbon-fibre composites extensively in their wings, fuselage and tail structures. However, adoption is not uniform across the market. The high-volume A320neo and 737 MAX are only around 15% composite, despite being the aircraft produced in the greatest numbers. The A220 is approximately 46% composite. This creates a substantial opportunity for the next generation of single-aisle aircraft to combine high composite content with much higher production volumes. The resulting weight reduction from increased composite use has knockon benefits in fuel consumption, range and emissions. The whitepaper uses aircraft interiors to illustrate the cumulative effect: it estimates that reducing aircraft weight by 100kg can save up to 7,500kg of fuel annually, corresponding to more than 23,700kg of CO2. Composites enable designers to produce large, lightweight and highly shaped structures that would be difficult or inefficient to manufacture from metal. The A320’s composite Sharklets are given as an example. By reducing wingtip vortices, they can deliver up to 4% lower fuel consumption. The low mass of composites is particularly valuable at the wingtip because weight there
Part one of the Composite materials in aeronautics whitepaper
has a disproportionate effect on wing bending loads. Looking ahead, the whitepaper identifies several areas requiring continued development if the composites sector is to meet the potential increased demand heading its way. High-rate and automated manufacturing will be key, as will repeatable production processes, inspection and non-destructive evaluation. Certification, recycling and end-of-life processing will also be crucial, alongside repair techniques and lower-carbon material systems.
MAJOR APPLICATION AREAS THE PAPER HIGHLIGHTS THREE MAJOR APPLICATION AREAS: • Interiors: glass-fibre composites and sandwich structures are used in overhead bins, sidewalls, lavatories, galleys, bulkheads and ceilings because they combine low weight with stiffness, durability and fire performance. • Engines: carbon-fibre fan blades and fan cases reduce mass, while ceramic matrix composites (CMCs) enable components to operate at temperatures where conventional metals struggle. • Primary structures: carbon-fibre composites are increasingly used in wings, spars, winglets, fuselage sections and tail structures.
www.engineerlive.com
37
FASTENERS & SEALING
®
®
S TAM P I N G S , WAS H E R S , S PAC E R S & S H I M S – MAD E TO O R D E R S I N C E 1919 z
ALL WE NEED ARE
YOUR SPECS WE'LL DO OUR PART. For over 100 years, nearly every industry across the globe has trusted Boker’s to provide quality components, worldclass service and fast delivery.
125
0.80
SUBMIT YOUR PART SPECS &
GET A FAST QUOTE scan or email
38
SALES@BOKERS.COM
www.engineerlive.com
+16127299365
bokers.com
FASTENERS & SEALING
Fluorescent adhesive demonstrates bonding
STRUCTURAL BONDING Kevin Brownsill, head of technical learning and development at Intertronics, discusses four considerations for selecting structural adhesives for performance and production
S
tructural adhesives can provide strong, load-bearing joints across a range of industrial and engineering applications. However, achieving reliable results requires more than choosing the ‘strongest’ material: process speed, substrate compatibility, production variability, automation requirements, and overall manufacturing costs must also be considered. Here, we consider four factors engineers should take into account when specifying a structural adhesive for high-performance applications.
guides and data sheets are useful for narrowing down the options, but they should not be relied on alone. Published properties are often measured under controlled laboratory conditions, which may differ significantly from those of the application. Practical trials and testing are therefore important, as is advice from an adhesives specialist with experience of how materials perform in different applications and conditions.
LOOK BEYOND THE DATA SHEETS
Substrate compatibility is fundamental to achieving a reliable bond. For an adhesive to wet a substrate effectively, it needs to have a lower surface energy than the substrate. High-performance plastics such as polypropylene and other polyolefins can be challenging to bond because their surface energies are typically low, often between 20 and 40dynes/ cm2. Where these plastics are selected
Polyurethanes (PUs), epoxies, and methyl methacrylates (MMAs) are among the main structural adhesive chemistries, offering a combination of adhesive and cohesive strength. Other potential options include cyanoacrylate adhesives (CAs) and single-part UVcuring acrylic adhesives. Structural adhesive selector
BOND LINE AND SUBSTRATE REQUIREMENTS
for their functional properties, surface preparation such as priming or plasma treatment may be necessary. The bond line itself also needs consideration. For larger bond areas, the adhesive’s gel time or pot life needs to allow sufficient time for dispensing or assembly before curing begins. Gap-filling requirements should also be assessed. Variations in moulded component dimensions can result in gaps ranging from zero to several millimetres within the same assembly, affecting the amount of adhesive required. Adhesive rheology is another factor. A thixotropic or low-viscosity adhesive, for example, will behave differently depending on the geometry of the bond line and the method of application. Bringing an adhesive specialist into the design process early on can help address these factors before the substrate and bond line is finalised. Leaving adhesive selection until later can restrict the available options
www.engineerlive.com
39
FASTENERS & SEALING
and make it harder to meet all the application requirements.
CONSIDER THE MANUFACTURING PROCESS
Adhesive selection is as much a manufacturing process decision as a chemistry one, and trade-offs must be factored in. Considering this from the outset allows the adhesive and application process to scale with production. For instance, while an epoxy may be desirable given its high strength, a manufacturer may have to accept its relatively slow room-temperature cure. Two-part adhesives with faster cure times can begin to gel within the mixing nozzle if they are not dispensed continuously or regularly purged. Single-part UV-curing adhesives, meanwhile, can provide rapid, ondemand curing and reduce the time components need to remain fixtured. While it may seem like a small factor, the packaging the adhesive is supplied in can have an important impact on the process, and therefore the selection of a material. A 10g container, for example, may be unsuitable where automated dispensing is required. Manual application can also be supplemented with dispensing UV adhesive curing
40
www.engineerlive.com
A dispensing gun used within structural bonding applications
equipment, benchtop robots or full Archytas automated work cell systems to increase accuracy, repeatability and throughput.
THINK CAREFULLY ABOUT COST
Does the adhesive you have chosen make commercial sense? It might be technically perfect but expensive enough to damage profitability. Similarly, selecting the cheapest adhesive is not necessarily the most economical approach either. An inexpensive adhesive may require more processing time, labour
or equipment, ultimately increasing the cost of each finished part. The commercial calculation should therefore analyse the overall cost per finished part. including the adhesive, assembly process time and complexity, and the labour cost. Structural adhesive selection is no straightforward task. Nonetheless, looking beyond the data sheet, balancing process and commercial realities with technical performance, and involving an adhesives specialist can help manufacturers to develop a reliable bonding process that remains practical as production scales.
HANDLE IT
FASTENERS & SEALING
42
www.engineerlive.com
SPIROL’s Christie Jones shares an innovative case study on how overhauling the design of free-fit hinge pins for medical device handles saved costs and retained performance
A
leading surgical device manufacturer was using seven different machined solid pins as free-fit axles in a surgical stapler assembly. The pins were slip-fit into place and retained by a plastic shroud that completely enclosed the outside of the medical device. The machined solid pins were specified with an outer diameter (OD) tolerance of ±0.0127mm (.0005”) and a length tolerance of ±.003” (0.076mm). The pin material was specified as X8CrNiS18-9 (1.4305) / AISI 303 (UNS S30300) austenitic stainless steel (SST). Since this grade of stainless steel is most readily available in bar stock, the material specification, combined with the tight dimensional tolerances, essentially dictated that the pins be machined rather than manufactured using a significantly less expensive production method such as cold heading.
FASTENERS & SEALING
THE COST-SAVING SOLUTION
SPIROL’s cold headed solid pin
SPIROL’s application engineering team conducted a thorough review of the performance requirements and determined that the tolerances specified for both length and diameter were significantly tighter than necessary, given that the pins served solely as free-fit hinge pins in the surgical device. In other words, the original specifications were adding significant manufacturing cost without providing any functional benefit to the assembly. SPIROL posed a simple question to the medical device manufacturer: “If you could save millions of pounds on the cost of the pins used in this surgical device, with no change in assembly performance, by allowing wider dimensional tolerances on the diameter and length, would you be interested?” Of course, they were. SPIROL Engineering recommended widening the diameter tolerance from ±0.0127mm (.0005”) to ±0.025mm (.001”) and the length tolerance from ±0.076mm (.003”) to ±0.25mm (.010”). To
put this into perspective, even though the allowable length tolerance was more than tripled, the difference is only about the width of two to three human hairs. SPIROL also recommended changing the material from X8CrNiS18-9 (1.4305) / AISI 303 (UNS S30300) stainless steel, to X4CrNi18-12 (1.4303) / AISI 305 (UNS S30500) stainless steel. While both grades are austenitic stainless steel, the change to 1.4303 / 305 stainless steel, combined with the wider diameter and length tolerances, enabled the pins to be cold headed from commercially available wire rather than machined from bar stock without compromising the fit, function, or performance of the assembly. By replacing the seven machined solid pins with cold headed solid pins, the medical device manufacturer realised annual savings of more than £2.2 million.
Christie Jones is at SPIROL: www.spirol.com
DS-DEC18-GEORGE EMMOTT CLOCK:DS-DEC18-GEORGE EMMOTT PRESSINGS 05/12/2018 11:46 Page 1
www.engineerlive.com
43
MOTORS, DRIVES & CONTROLS
ESP motor control solutions have progressively evolved from generic control approaches toward application-driven solutions
CONTROLLED LIFTING Motaz Hassan, global application manager – artificial lift solutions at ABB, explains why motor control is the key starting point for optimising ESP installations
W
hen natural reservoir pressure is insufficient, artificial lift systems incorporating Electrical Submersible Pumps (ESPs) play a vital role in maintaining the flow of fluids from oil wells. ESP systems must operate under continuously changing conditions including declining reservoir pressure, variable gas content, producing solids, changing fluid properties, and eventually fluctuating load demand. Applications must respond to dynamic loads, rather than the steady-state conditions found in most industrial processes. The pump motor is required to operate across a wide range of speeds
44
www.engineerlive.com
and loads, often under unstable conditions. The variable speed drive (VSD) that controls the motor must deliver consistent performance in inconsistent environments. This calls for the VSD to function as more than a speed control device; its embedded control logic must provide smooth start and acceleration behaviour, stable operation during load variations, response to supply and load disturbances, process changes and balance between protection and production continuity. In addition, accumulated field experience enables the development of application-specific control programmes that can improve usability, enhance
safe operation, protect equipment, and support production optimisation. ESP installations are increasingly adopting permanent magnet (PM) motors to improve efficiency and performance. This requires advanced drive control to ensure precise and robust startup, synchronisation, efficiency, management of regenerative behaviour during backspin conditions and stable control across varying operating conditions.
TACKLING BACKSPIN
Backspin occurs should the pump stop and the fluid column drives the system into reverse rotation. The magnitude of ESP backspin torque and the resulting speed is determined by reservoir and
MOTORS, DRIVES & CONTROLS
SMC-DRIVEN FUNCTIONS ABB’s SMC delivers application-oriented motor control
well conditions, the fluid properties, the height and load of the fluid column, as well as the design and construction of the pump itself. All these variables dictate the behaviour of the ESP system during shutdown and how aggressively it may rotate in reverse. This, in turn, directly impacts the complexity and risk associated with restarting the ESP safely. To avoid backspin, the VSD has to detect the rotational status of the motor, prevent unsafe restart attempts, and manage controlled synchronisation before torque is applied. A stable and controlled restart is essential both to protect the equipment and maintain production continuity.
SUCCESSFUL RESTARTS
Downhole mechanical issues can cause difficulties for ESP systems in ensuring continuous operations or achieving a successful restart. A common cause is solids present in the fluid, or harsh operating conditions. These factors can increase torque demand, eventually leading to a full stalled condition if the pump becomes stuck or triggers an overload trip. Preparing for a successful restart requires dedicated motor control capabilities within the drive so that the pump is released in a controlled manner. Effective management of this recovery phase effectively is vital to minimise additional mechanical stress and avoid repeated trip conditions. Managing underload conditions covers a different set of challenges. There can be a negative influence on downhole pump and motor cooling efficiency because the motor relies on fluid flow for proper heat dissipation. Persistent underload conditions can indicate mechanical issues such as broken shafts or partial loss of pump stages. If not addressed, they can ultimately lead to long-term degradation or permanent failure if not properly addressed.
OVERCOMING GAS LOCKS
Many wells, especially those with high gas content, can experience gas locks that significantly affect ESP performance and create underload conditions. The risk is increased in installations where there is limited or no gas separation or handling equipment. The result can be the pump losing its ability to lift fluid, causing unstable operation and reduced production efficiency. Advanced motor control capabilities are required within the drive to continuously monitor operating parameters and adapt motor behaviour accordingly.
APPLICATION-DRIVEN ESP MOTOR CONTROL ESP motor control solutions have progressively evolved from generic control approaches toward application-driven solutions that incorporate dedicated functionalities. A good example is the Submersible Motor Control Programme (SMC) implemented within ABB’s ACS880 drive platform. SMC is focused on delivering application-oriented motor control to ensure stable performance across a wide operating range, while also integrating key protection functions. It also supports a simplified and robust system architecture, reducing overall complexity without compromising performance or reliability. Dynamic oilfield conditions present significant challenges for ESP systems in maintaining stability, protection and performance. Adopting intelligent motor control through a drive with dedicated built-in functionality can transform these challenges into controllable outcomes.
• Kick-start & acceleration assistance: This uses current-boost-based start functions to provide sufficient torque for a PM motor at low speeds. It enables reliable startup and smooth acceleration under high load conditions without losing synchronisation • Energy optimiser mode: This automatically optimises motor current using a Maximum-Torque-PerAmpere (MTPA) approach. It improves power factor and energy efficiency especially at partial loads compared to conventional scalar control • Backspin speed observer: The sensorless observer detects motor speed and direction during backspin to enable safe startup by avoiding operation against reverse rotation. This prevents torque reversal, reduces the risk of trips, and minimises mechanical stress • Flying start: This enables the ESP to restart in a backspin condition by synchronising with the motor’s speed and direction. It ensures smooth restart in the correct direction while avoiding mechanical stress and high inrush currents • Pump impeller cleaning: Applying controlled motion sequences can safely remove solids buildup in pump stages. This restores performance while reducing the risk of stall, instability, mechanical failure, and downtime • Gas lock and underload protection: This function detects gas lock conditions and dynamically adapts motor behaviour to restore flow, stabilising operation and reducing manual intervention in gas wells • Production optimisation (PID Control): Built-in PID control continuously adjusts the motor speed based on process feedback, maintaining optimal operating conditions and maximising production efficiency • Automatic restart: The ESP can recover quickly from transient trips by automatically restarting the drive under actual operating conditions
www.engineerlive.com
45
MOTORS, DRIVES & CONTROLS
Companies that reduce complexity shorten development time, lower error risk and increase uptime
Digitalisation creates value only when it rests on an operational base that is simple, robust and transparent
SIMPLE ADVANTAGE Lenze’s Marc Vissers explains why Europe’s next phase of digitalisation depends on simpler systems, scalable knowledge and stronger operational foundations
E
urope does not need more automation complexity. It needs operational choices that make performance easier to scale. Across Europe’s manufacturing industry, leadership teams are being asked to deliver more with less: higher output, smaller batch sizes, lower energy exposure and greater flexibility for customers. Yet many operational environments have become harder to manage than they were ever meant to be. As a result, growth, maintenance and innovation are increasingly difficult to scale. Europe’s industrial competitiveness will increasingly depend on how well manufacturers turn complexity into
repeatable, scalable performance. For machine builders, system integrators and industrial decision-makers, the discussion is no longer about the next automation choice alone. It is about whether the operational foundation still supports the speed, resilience and cost discipline the market now demands. That is why the conversation is moving from technology selection to business performance. Digitalisation creates value only when it rests on an operational base that is simple enough to scale, robust enough to protect continuity and transparent enough to support better decisions across the lifecycle. For years, operational technology
was seen mainly as an engineering domain: essential, technical and operational. That view is no longer sufficient. Energy uncertainty, labour shortages, loss of experienced domain knowledge and sharper capital discipline have made the factory a strategic business asset. The factory is where financial resilience, delivery reliability and strategic flexibility are either protected or exposed. Complexity, downtime, energy loss and knowledge dependency now directly affect margins, customer commitments and strategic agility. The real question is not whether companies should continue to
www.engineerlive.com
47
MOTORS, DRIVES & CONTROLS
digitalise. It is whether their operational foundation is strong enough to convert digitalisation into measurable business value.
THE TRUE VALUE OF DATA
In many factories and machine platforms, that foundation has grown over time: systems alongside systems, variants alongside variants, customisation on top of customisation. The biggest weaknesses are rarely found in a single machine or technology. They usually sit in the system around it: too many customer-specific exceptions, limited standardisation, fragmented software and service processes, and knowledge concentrated in a small group of specialists. Even decisions that appear technical, such as selecting the right axis concept, increasingly influence how easily performance can be repeated, maintained and scaled. At first glance, this may look flexible. In practice, it raises maintenance costs, limits engineering capacity and makes downtime more visible as a financial risk. The next productivity step will not come from adding another technology layer, but from the discipline to simplify, standardise and modularise: choosing
the best-fit axis, architecture and control concept for the business outcome, not simply the most familiar technical option. Companies that reduce complexity shorten development time, lower error risk, increase uptime and make growth less dependent on scarce capacity. In a labour-constrained market, the issue is not only the shortage of people; it is the growing concentration of critical domain knowledge. The answer is not to place more pressure on scarce specialists. It is to capture their expertise in standards, modules and repeatable concepts, so knowledge becomes scalable, transferable and less dependent on individual availability. The parallel with grid congestion is telling. Across Europe, capacity constraints have shown that technical fixes alone do not solve structural pressure. The stronger question is which operational choices safeguard continuity, reduce risk and protect the business case in a measurable way.
AUTOMATION SHIFT
Investment discussions must therefore move beyond purchase price and towards total cost of ownership. Energy consumption, maintenance, downtime, service, upgrades and Marc Vissers is at Lenze: www.lenze.com Productivity depends on choosing the best-fit axis, architecture and control concept for the business outcome
48
www.engineerlive.com
flexibility determine return. This is where the difference becomes visible between companies that sell technology and companies that help organise value. Lenze approaches this challenge from that second perspective. By engaging early, the underlying business questions become visible: where vulnerability arises, where margin disappears and where variation limits scalability. From that analysis, complexity can be reduced, architectures can be standardised and technology can be translated into a lifecycle- and TCO-driven business case. The result is not simply a stronger technical story. It is a more controllable business case: fewer variants, lower lifecycle costs, more predictable performance and faster scalability. Above all, it reduces dependence on exceptions, scarce resources and isolated domain knowledge. Tomorrow’s winners will not be defined by the amount of technology they deploy, but by how effectively they connect technology to what matters in the boardroom: cost control, continuity and scalable value. In Europe’s next phase of digitalisation, the strongest manufacturers will be those that simplify best.
MOTORS DRIVES & CONTROLS
Smart synergy sparks intelligence.
The clever integration of industrial AI with solutions for drive and sensor technology, software, and industrial communication is driving automation forward with unerring precision. Track down a world of possibilities at the SPS – Smart Production Solutions, the international trade fair for automation.
Create the Future with Automation
24 – 26.11.2026 NUREMBERG, GERMANY
Spot the World of Industrial AI See you at the SPS!
sps-exhibition.com
SDT Cyclo 100 Advert (185 x 121mm) EN 1.indd 1
18/03/2025 10:35:46
www.engineerlive.com
49
SKILLS ZONE Black & White Engineering’s graduates and apprentices are based worldwide
GROWING GRADUATES Black & White Engineering has expanded its apprenticeship workforce to meet increased demand for engineering skills across critical infrastructure
G
lobal design consultancy Black & White Engineering has grown its global graduate and apprenticeship workforce to 217 people, in response to the need for engineering skills across data centres and other critical infrastructure markets. Graduates and apprenticeships now make up 17.3% of the business, with nearly one in every six employees on a structured development pathway. The consultancy welcomed 137 graduates and apprentices last year as it continues to invest in longterm training routes at a time when employees are under pressure to build stronger skills pipelines.
GLOBAL REACH
Black & White Engineering’s graduates and apprentices are based worldwide, with teams in Dubai, Dublin, Edinburgh, Gurugram, London, Manila, Newcastle, Noida and Riyadh. The programme offers upskilling routes across disciplines such as electrical, mechanical, civil, computational fluid dynamics (CFD), sustainability engineering, BIM and learning and development. “Graduate and apprenticeship development is a significant part of how we build and future-proof the business,” says Caff Allen, global director of learning & development at Black & White Engineering. “Welcoming 137 people into these routes shows the scale of our investment in our people, but the more important point is the type of experience they are getting. They are working with experienced colleagues, learning on live projects, and building
50
www.engineerlive.com
The consultancy offers international work experience
the skills needed to support complex, mission-critical buildings and infrastructure.” The company’s training routes are designed to give its employees practical experience of technical work, client requirements and multidisciplinary project teams. The programme includes structural support from line managers, mentors and senior colleagues, alongside training in technical and professional skills. Graduates and apprentices also take part in development events designed to broaden their experience beyond technical engineering. “The engineering skills challenge will not be solved by recruitment alone,” continues Caff. “Businesses need to give people options for developmental routes into the industry, clear responsibility and the support to develop over time. Our graduate and apprentice programmes are built around that. They give people the chance to contribute early while learning how engineering decisions affect design quality, delivery and long-term performance.”
GATHERING TOGETHER In October, nominated Black & White
Graduates at the consultancy’s Manila design hub
Engineering graduates will be able to attend the company’s Graduate Global Gathering in Boracay, Philippines. The event will bring together graduates from across the firm’s international teams in order to strengthen relationships across its future workforce. “Bringing our graduates and apprentices together through events like our Technical Excellence and Innovation Conference, and the Graduate Global Gathering, helps create connections and ideas that will shape both their careers and the future of our business,” Caff says. The consultancy also offers international work experience where graduates and apprentices in its front office can spend time working with their colleagues based in the Global Design Hub in Manila. Caff adds, “For Black & White Engineering, developing graduate and apprentice talent is part of long-term workforce planning. As demand grows across data centres and other missioncritical sectors, we need people who understand both the detail of design and the pace of delivery. That starts with giving them the right exposure, mentoring and training at the beginning of their careers.”
SKILLS ZONE Bytesnap Design graduate, Roberto Holmes
ELECTRONICS ENGINEERS IN DEMAND ByteSnap Design shares five ways electronics employers can attract the next generation of talent
D
espite years of discourse around the engineering skills gap within the electronics industry, there is little sign of the challenge easing. According to the Institution of Engineering and Technology (IET), 76% of engineering employers report difficulties recruiting for key roles. Looking ahead, the institution’s 2025 UK engineering and technology skills survey says 42% of employers identified innovative thinking as the most important skill for business growth over the next five years, followed by technical and engineering skills (39%) and specialist digital skills and knowledge (39%). Electronics design company ByteSnap Design has spoken to four of its graduate and early-career engineers about their journey from university into embedded systems.
RECRUIT FOR POTENTIAL
ByteSnap Design says the strongest message from its interviews is that employers should not expect graduates to arrive with every practical skill in place. The firm’s engineers describe their university degrees as providing the theoretical foundation upon which professional engineering could be built. Much
of their experience of embedded software, firmware development and hardware interfaces came through placements, independent projects or learning outside formal teaching. ByteSnap Design says, therefore, that graduate recruitment should focus on identifying people with the aptitude to become excellent engineers rather than expecting candidates to have already acquired commercial experience, and that curiosity, resilience and a willingness to learn are every bit as valuable as technological knowledge at the point of recruitment.
LOOK BEYOND ACADEMIC RESULTS
Projects, placements and extracurricular engineering activities frequently became the centrepiece of technical conversations because they allowed candidates to explain how they approached problems, justified design decisions and responded when things did not go to plan. Within ByteSnap Design’s recruitment process, several engineers described interviews that encouraged discussion rather than simply testing whether candidates could produce the right answer under pressure. They felt this approach allowed them to demonstrate curiosity, logical
thinking and communication skills alongside technical knowledge.
DEVELOPMENT SHOULD BE PART OF RECUITMENT MESSAGE
According to ByteSnap Design, its engineers emphasised wanting opportunities to learn, tackle new technical challenges and continue developing once they joined industry. Several highlighted the appeal of working across different sectors and technologies within an embedded software and electronics consultancy, allowing them to broaden their experience rather than becoming highly specialised at the start of their careers. Others reflected on the value of mentoring, supportive colleagues and the opportunity to take increasing responsibility as their confidence grew.
CULTURE IS IMPORTANT
For graduate engineers, the first employer often shapes the early stages of an entire career. They are therefore assessing culture, support and opportunities for learning from their first interaction with a company. Organisations that demonstrate collaboration, openness and investment in their people during recruitment may be better placed to attract graduates who have multiple career options available to them.
SHOW THE POSITIVES
Graduates entering the workforce today can choose from a wide range of industries, many of which actively target the same technical skills. Electronics companies therefore need to articulate what makes the sector distinctive rather than assuming graduates will automatically understand its appeal. For the engineers interviewed, that meant working on products that interact with the physical world, solving complex technical challenges and contributing to projects across multiple industries. The combination of software, hardware and real-world engineering problems was a significant attraction and something they felt differentiated embedded systems from many other software careers.
www.engineerlive.com
51
SHOW PREVIEW
F
AM TAKES CENTRE STAGE IN FRANKFURT
ormnext returns to Frankfurt am Main from 17–20 November 2026, bringing together more than 800 exhibitors and 38,000 visitors for four days focused on the latest developments in industrial Additive Manufacturing (AM). Positioned as a central hub for the AM industry, Formnext will showcase technologies spanning the entire production process chain. Alongside industrial 3D printing systems, visitors can explore advances in materials, automation, software, post-processing and quality assurance, providing insight into how AM is progressing from specialist production technology towards wider industrial adoption. The event’s supporting programme will address both current engineering challenges and future opportunities. The AM Innovation and Standards Summit, organised by ASTM, will
examine certification and standards, while the Formnext Defence Summit will explore the role of AM in developing resilient security applications. The BE-AM Symposium will focus on developments in additive construction, while showcases and guided tours will highlight advances in post-processing. Innovation will also feature prominently through the Formnext
Image via Mesago Messe Frankfurt/ Marc Jacquemin
Awards, recognising developments across the industry, alongside the Start-up Area and Pitchnext event, which provide a platform for emerging AM companies and technologies. This year’s programme will also include a focus on the UK as Partner Country, as well as VDMA and BE-AM showcases, Discover3DPrinting seminars and a dedicated Career Area. With AM technologies evolving rapidly across sectors, Formnext provides an opportunity for engineers, manufacturers and technology developers to assess emerging solutions, exchange expertise and explore practical routes towards greater industrial use of additive production. For more information visit: www.formnext.mesago.com/ frankfurt/en/expo
INDUSTRIAL AI IN FOCUS AT SPS
T
he SPS 2026 exhibition will return to Nuremberg from 24–26 November 2026, bringing together around 1,000 exhibitors from across the globe to showcase the latest developments in smart and digital automation. Spanning the complete automation spectrum, the event will provide engineers and industry professionals with an opportunity to experience emerging technologies through live demonstrations, practical applications and expert presentations. This year’s key topic is Industrial AI, highlighting how AI is becoming increasingly integrated across automation technologies, including drive systems, sensors, software and industrial communications. Industrial AI is moving beyond experimentation into practical manufacturing applications. At SPS 2026, visitors will be able to explore its use in engineering workflows, intelligent control devices, predictive maintenance, quality assurance
52
www.engineerlive.com
and adaptive production control. The growing role of physical AI will also be examined, with technologies offering potential improvements in efficiency, flexibility and resource utilisation. Image via Mesago Messe Frankfurt/Arturo Rivas Four dedicated stages will host expert hands-on experience with machines presentations covering current and industrial technologies. With automation trends, technologies and global market leaders exhibiting real-world applications, providing alongside emerging technology insights for developers, decisiondevelopers, SPS 2026 promises a makers and emerging engineering broad view of how automation is talent. Joint stands will offer evolving. opportunities to discover automation solutions, connect with start-ups and explore areas including IT integration For more information visit: and industrial security. www.sps.mesago.com/ The event will also feature dedicated nuernberg/en activities for young talents, providing
SHOW PREVIEW
SHOWCASING TURKEY’S COMPOSITE SECTOR
T
URKCOMPOSITE will bring together manufacturers, technology providers, engineers, procurement professionals and industry decisionmakers for a comprehensive showcase of Turkey’s composites sector 21-23 October 2026. Organised by CNG Expo Events in cooperation with the Turkish Composites Manufacturers Association (KSD), the event covers the complete composites value chain, from raw materials and manufacturing technologies to automation and advanced engineering solutions.
A
The exhibition will focus on composite technologies serving strategic industries including defence, aerospace, automotive, rail, marine, wind energy, construction and industrial manufacturing. With a target of approximately 100 exhibitors and 10,000 professional visitors, TURKCOMPOSITE aims to provide a platform for technology exchange, business development and international networking. Turkey’s position within the global composites market will be a central theme. The country combines
established industrial infrastructure, a skilled workforce and a developed supply chain, while its geographical location provides access to European, Middle Eastern, African and Asian markets. According to 2024 data supplied by the organisers, composite material consumption in Turkey reached 270,000 tonnes annually, highlighting the scale and potential of the domestic market. For more information visit: www.turkcomposite.com
CONNECTING INNOVATION WITH INDUSTRY
dvanced Engineering 2026 returns on 4–5 November, bringing together more than 9,000 engineering professionals, 400 leading suppliers and over 200 industry speakers at the UK event focused on industrial innovation. Covering sectors including aerospace, automotive, space, rail, maritime, energy and electronics, the event provides engineers, buyers and technical specialists with opportunities to compare technologies, discover new suppliers and explore solutions to complex manufacturing challenges. Key themes include industrial
Index to advertisers ASC Sensors
21
Bokers
38
Cirrus Research
36
Emmott Springs
43
Formnext Frankfurt
5
resilience, supply chain security, sovereign capability and the transition towards net-zero engineering. A diverse programme of dedicated pavilions will provide focused access to specialist technologies and expertise. The Composites UK Pavilion, for example, will feature around 18 companies from the UK composites sector, while pavilions from ADS, Make UK, GTMA and the Surface Engineering Association will showcase aerospace, defence,
precision engineering and surface technologies. The Composites Networking Lounge will host industry sessions spanning aerospace, motorsport, automotive, medical, defence and renewables. Meanwhile, the Auto & Aero Networking Lounge will showcase smart tooling and advanced assembly solutions. The Skills Junction will address the engineering and manufacturing skills gap by bringing industry, education and other stakeholders together.
For more information visit: www.advancedmanufacturinguk.com
JEC World 2027
OBC
Plastic Coatings
31
Lee Spring
IFC
PEI Genesis
IBC
Lenze
46
RECOM dc/dc
21
LMI TECHNOLOGIES
22
RECOM racpro1
18
MARL International
22
Spirol
38
McCarthy Environmental
28
SPS
49
Nordson
18
Star Fasteners
41
Sumitomo Drives
49
TLX Technologies
13
North Composites Engineering
36
www.engineerlive.com 53
GET INVOLVED e advertising@setform.com t +44 (0)207 253 2545
YOUR GUIDE TO DISTRIBUTORS, SUPPLIERS AND MANUFACTURERS IN THE INDUSTRY
Boker’s Inc.
Gold & Wassall Hinges
HIOKI
Boker’s, Inc., is a full-service manufacturer of precision metal stampings, washers, spacers and shims. Since 1919, nearly every industry around the world has trusted Boker’s to provide quality made-to-order components, world-class service and fast delivery.
With over two centuries of experience in the hinges industry, Gold and Wassall provides a fully comprehensive design and manufacturing service for any kind of hinge for practically any application.
HIOKI, founded in Japan in 1935, leads precision test and measurement technology. Renowned for advanced electrical current sensors, power electronics, and battery solutions, we deliver uncompromised accuracy and innovation built and engineered in Japan.
T +1 612 729 9365
T +44 (0)1827 63391
T +49-(0)6196-76515-0
E sales@bokers.com
E enquiries@goldwassallhinges.co.uk
E hioki@hioki.eu
W bokers.com
W goldwassallhinges.co.uk
W shop.hioki.eu/
Lenze
LMI Technologies
North Composites Engineering
Lenze is a global automation specialist supplying drive, control and software solutions for machine builders. Its electromechanical and automation technologies support efficient industrial machinery across the lifecycle, from design and commissioning to operation and optimisation.
As the global leader in 3D scanning and inspection, LMI Technologies works to advance quality and productivity with 3D sensor technology.
A highly professional company who over the last 14 years have trained and actively empowered the composite sector. Experts in composite services, we provide world class training, consultancy and equipment to the Aerospace, Marine, Wind Turbine and Automotive sectors.
T +44 (0) 1234 753200
T +44 (0) 1942 665292
E sales.uk@lenze.com
E contact@lmi3d.com
E info@northcompositesengineering.co.uk
W www.lenze.com
W lmi3d.com
W www.northcompositesengineering.co.uk
PCE Instruments
RECOM Power
Rutland Plastics
Develops, manufactures and distributes test instruments, scales and balances and selected laboratory equipment for industry, trade and research. In addition to pre- and after-sales support, calibration and repair are also offered.
RECOM produces standard and custom DC/ DC, AC/DC converters, switching regulators, and LED drivers from sub-1W to tens of kW. Headquartered in Gmunden, Austria, RECOM is known for quality, innovation, wand excellent customer service.
With 70 years of experience, we offer a full range of plastic injection moulding services across all sectors with the ability to make plastic parts from 1g to 45kg and up to 1.5m in size.
T +44 (0) 161 464902 0
T +43 7612 883 25 700
T 01572 723476
E info@pce-instruments.co.uk
E info@recom-power.com
W www.pce-instruments.com
W recom-power.com
E enquiries@rutlandplastics.co.uk W www.rutlandplastics.co.uk
www.engineerlive.com
xx
MIL-STD-1553BCompliant Solutions In Stock Now at PEI-Genesis
CABLE ASSEMBLIES
DATA BUS COUPLER ADAPTER
CONNECTOR
WWW.PEIGENESIS.COM PEI-Genesis is one of the world’s fastest assemblers of precision connectors and cable assemblies. From the largest connector component inventory in the world, they develop engineered solutions that support the military, industrial, medical, aerospace, transportation, and energy sectors worldwide. Headquartered in Philadelphia, PA, PEI-Genesis has production facilities in South Bend, IN; Southampton, UK; and Zhuhai, China, as well as sales offices throughout the Americas, Europe, and Asia.
TERMINATOR
IGN DES CE A & P RE OS N AER ITECTU CTIO H E U C V R R I T T A ONS OMO AUT ING & C D BUIL NSE ES E S IANC DEF TRICAL L P AP C ELE TRONIC C ARE ELE TH C Y L A R HE HINE C A M INE MAR GAS S & OIL RGIE YS E A N W E E R A I L WA B L E ISUR E E N L E R & TION RT S S P O S P O RTA R I E S N ST TRA R INDU E WAT