January 2026 SUBSCRIBE FOR FREE
www.engineerlive.com
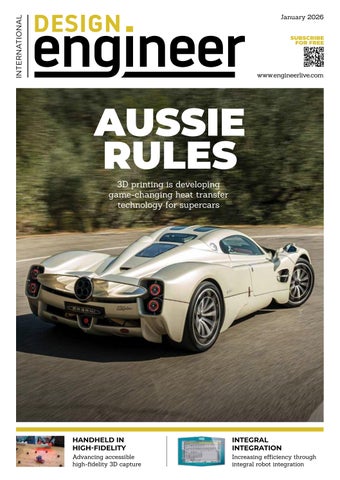
AUSSIE RULES 3D printing is developing game-changing heat transfer technology for supercars
HANDHELD IN HIGH-FIDELITY
INTEGRAL INTEGRATION
Advancing accessible high-fidelity 3D capture
Increasing efficiency through integral robot integration
Signal Capture and Creation – made easy! Connect via Ethenet/LXI to any PC, Laptop or Network Install the divers (Windows or Linux) and stat! SDKs (C/C++, Python, MATLAB, LabVIEW etc.) and poweful software tools included
tb D i g i t i ze r N e
oxe s
ultrafast as 5 MS/s to From as low ants, offer 95 vari 10 GS/s, we anted rpay for unw e v o ’t n o d u so yo idths. ds or bandw e e sp , ls e n n cha
t b oxe e N r o t a r e n Ge
s
Generators ry Waveform ra it rb A se e h T lly any uce practica (AWGs) prod cise and xtremely pre waveform. E g single .g. for mov in low-noise, e h. ntum researc atoms in qua
igitiz D + r o t a r e n Ge
er
ox! itizer in one b ig D + G W A l d-loop Multi-channe nse and close o sp re slu u Ideal for stim S/s S/s to 1.25 G applications! SPEED 40 M
r 8+8 2+2 or 4+4 o LS E N N A H C 14 to 16 bit RESOLUTION dels different mo VARIANTS 14
BOX hybridNET
/s to 10 GS/s SPEED 5 MS 1 to 48 CHANNELS 8 to 16 bit RESOLUTION odels 5 different m VARIANTS 9
digitizerNE
TBOX
/s S/s to 10 GS SPEED 40 M 1 to 48 CHANNELS 16 bit RESOLUTION odels 7 different m VARIANTS 4
generatorN
t D D S - G e n e ra
ETBOX
ors
Each DDS one channel! n o s re o c S quency, Up to 50 DD mmed for fre ra g ro p e b n ave) ca litude core (sine w ope and amp sl y c n e u q e fr hase, instead of amplitude, p commands – le p m si w fe st a slope with ju tions. array calcula ta a d e rg la making Hz ENCY 200 M MAX. FREQU 1 to 24 CHANNELS 16 bit RESOLUTION dels different mo VARIANTS 12
generatorN
ETBOX
SPECTRUM I N S T R U M E N T A T I O N
Perfect fit – modular designed solutions www.spectrum-instrumentation.com | Europe / Asia: Phone +49 (4102) 695 60 | US: Phone (201) 562 1999
CONTENTS
Welcome Design engineering is entering a phase where boundaries between materials science, manufacturing and system integration are increasingly blurred. Few areas illustrate this better than the rapid convergence of additive manufacturing, advanced materials and electrified vehicle design. In 3D printing, engineers are now exploiting additive processes to deliver functional, load-bearing components with repeatable quality – our cover story on page 6 goes into further detail. Multi-material printing, high-temperature polymers and metal AM (page 12) are enabling part consolidation, internal lattice structures,. while design-for-additive principles are becoming embedded earlier in the development cycle (page 20). Material innovation continues to be a powerful catalyst (page 11). Self-healing polymers, biobased resins and high-performance thermoplastics are moving from the lab into real-world applications (page 32). In parallel, advances in composite automated fibre placement, recyclable matrices and hybrid composite-metal structures are addressing cost, scalability and sustainability - key considerations for automotive and aerospace engineers alike (page 27). Battery design in the automotive sector is also undergoing fundamental change (page 24). Structural battery packs, solidstate chemistries (page 8) and new thermal management strategies are forcing closer collaboration between electrical, mechanical and materials engineers, fostered largely by upcoming industry events (page 48). Hayley Everett Editor
6
JANUARY 2026 COVER
SPECIAL FEATURE: DIGITAL TWINS
6
14
Aussie Rules U sing 3D printing to design game-changing heat transfer technology for supercars
A new era for simulation Enabling faster innovation through advanced simulation and AI
AUTOMOTIVE DESIGN
INSTRUMENTATION & ELECTRONICS
8
16
A solid approach Solid-state battery design enters an inflection point
ADDITIVE MANUFACTURING
11 12
Adaptive twisting metamaterials A 3D printed breakthrough for next-generation vehicle crash protection
Handheld in high-fidelity Introducing Hexagon’s latest advancement in handheld metrology
20
Coming of age
How generative design is reshaping engineering workflows
Breaking manufacturing barriers How 3D printing is powering scalable production
16 www.engineerlive.com
3
CONTENTS
MATERIALS • PROCESSES • FINISHES
MOTORS, DRIVES & CONTROLS
22
40
Aluminium alternative
How thermally conductive plastics can offer a more sustainable and performance-optimised choice over aluminium
24
Beyond limits
A high-voltage cathode breakthrough for next-generation batteries
Integral integration
How to achieve increased efficiency through integral robot integration
42
Reliable robots
Designing battery systems that support reliable robotic performance
SKILL ZONE COMPOSITES
27
Sustainable at scale
High-volume composite braiding and circular design in structural applications
44
46
Data reveals an acute shortfall threatening the UK’s technical workforce
SHOW PREVIEW
48
Connecting the composites community
JEC World takes place 10-12 March 2026
Building Britain’s battery workforce
Why skills will decide the future transition to electric vehicles
The apprenticeship gap
Innovation in industrial technology Southern Manufacturing & Electronics returns to Farnborough in February
30
Automating composite manufacturing
Airborne and Lockheed Martin advance digital automation for composite manufacturing
32
Biocomposite boom
How biocomposites are gaining industrial momentum
FASTENERS & SEALING
34
Talking tolerances
The advantages of oval compression limiters
37
Aeropaste adhesives Enabling next-generation aerospace bonding with paste adhesives
42
PUBLISHER Jerry Ramsdale EDITOR Hayley Everett heverett@setform.com DESIGN – Dan Bennett, Jill Harris HEAD OF PRODUCTION Luke Wikner production@setform.com HEAD OF SALES & PARTNERSHIPS David Pattison ACCOUNT DIRECTORS John Abey | Peter King SENIOR ACCOUNT MANAGERS John Davis | Darren Ringer | Roy Glasspool ACCOUNT MANAGERS Paul Maher | Iain Fletcher | Marina Grant e advertising@setform.com
Setform’s international magazines for engineers are published quarterly and distributed to senior engineers throughout the world. Other titles in the company portfolio focus on Oil & Gas, Design, Transport, Mining, Energy and Power. The publishers do not sponsor or otherwise support any substance or service advertised or mentioned in this book; nor is the publisher responsible for the accuracy of any statement in this publication. ©2026. The entire content of this publication is protected by copyright, full details of which are available from the publishers. All rights reserved. No part of this publication may be reproduced, stored in a retrieval system, or transmitted in any form or by any means, electronic, mechanical, photocopying, recording or otherwise, without the prior permission of the copyright owner.
CONTACT US... t +44 (0) 207 253 2545 e mail@setform.com
4
www.engineerlive.com
Setform Limited | 6 Brownlow Mews, London, WC1N 2LD, United Kingdom
AUSSIE RULES 3D printing is developing game-changing heat transfer technology for supercars
INNOVATION THROUGH COLLABORATION FROM DESIGN THROUGH PRODUCTION, TLX Technologies
works hand-in-hand with your design team to develop and produce custom solenoids and valves that solve your application’s most challenging problems. + Form factors that meet space constraints + Designs that minimize energy consumption + Solutions that withstand debris, vibration, and extreme temperatures and pressures + Solenoids with the force and stroke your application needs + Valves that deliver precise flow control, low pressure
CONTACT US ABOUT YOUR FIRE SUPPRESSION NEEDS. CONTACT US WITH YOUR CHALLENGE
sales@tlxtech.com | tlxfire.com sales@tlxtech.com | tlxtech.com
© 2026 2025 TLX Technologies
drop, and little or no hysteresis
COVER STORY
Conflux’s watercharge air coolers enabled Donkervoort to downsize its initial prototype package
Metal AM accelerated the design phase of Conflux’s work for Donkervoort
Conflux’s 3D-printed heat exchangers were integrated within the Pagani Utopia hypercar transmission
AUSSIE RULES Louise Davis reveals how a Victoria-based company is using 3D printing to develop game-changing heat transfer technology for supercars
W
hen former F1 design engineer Michael Fuller decided to apply his F1-grade mindset to road cars, he couldn’t have predicted how satisfyingly he’d be able to prove his new technology concept in the real world. In 2015 Fuller founded Conflux Technology, an advanced manufacturing company specialising in high-performance 3D-printed heat exchangers, in Geelong, Australia. By 2025, the company, via partnerships with several high-profile automotive players, was able to announce some astonishing results in 3D printed
6
www.engineerlive.com
thermal innovation. As the Australian innovator explains, one notable highlight is a project with Dutch sports car manufacturer, Donkervoort, on its soonto-be-unveiled P24 RS supercar: “We engineered a pair of ultralight water charge air coolers using computational fluid dynamics (CFD)-driven fin geometry, density and flow paths tuned to the P24 RS, cutting weight to about 1.4kg per unit [compared with 16kg for traditional systems] and enabling shorter intake routing, sharper throttle response and superior cooling versus the brief’s target.” Fuller reveals that exceeding the already challenging brief had
a positive knock-on effect: “Our approach was so effective that Donkervoort was able to further downsize the initial prototype package, contributing to the company’s lightweight design ethos.” Detailing the method behind these impressive results, Fuller says: “Metal additive manufacturing (AM) enables us to create gas-tight, thin walls and complex, evolving internal channels that conventional methods can’t produce, while eliminating tooling so rapid design iterations move at CAD speed, enabling us to deliver F1 grade cooling performance for highperformance road cars.”
COVER STORY
STEEL CITY SITE Conflux has recently opened a UK facility in Sheffield. On this, Fuller comments: “Europe accounts for over 35% of our business, so Sheffield gives us local, same time zone support and proximity to key programmes. The site will initially expand our in house testing (including two phase heat exchange) and drive product and material parameter development, with tighter collaboration cycles alongside European customers and programmes such as TheMa4HERA (an EU Clean Aviation program to develop hydrogen-electric regional aircraft).” The UK site is also part of Fuller’s future-proofing plans: “As regional demand grows, we’ll scale the hub into our full Conflux Production System, enabling localised, resilient supply chains for our customer’s heat exchangers. This roadmap lets European partners move faster into production using commercially available production equipment.”
ITALIAN EXCHANGE PROGRAMME
Another example of such work can be found within a successful six-year partnership to integrate Conflux’s 3D-printed heat exchangers in the Pagani Utopia hypercar transmission – delivering a model that’s 30% more efficient than conventional designs. “We achieved the 30% heat rejection gain by replacing the incumbent with a drop-in cartridge heat exchanger featuring optimised coolant inlet/ outlet geometry, our proprietary fin designs and ultra fine 0.26mm fin gaps to improve flow distribution and reduce oil side pressure drop, all within the original transmission envelope,” explains Fuller, who has recently transitioned from Conflux’s CEO to executive chairman.
Michael Fuller, executive chairman at Conflux
Commenting on the design process, Fuller says: “The development spanned several months with up to eight full-size prototypes, underpinned by extensive CFD to balance heat rejection against pressure losses. The parts were validated through ISO 17025 thermal-fluid testing, 15,000km of road/track trials and non-destructive inspections using ANSTO Synchrotron (Australia’s synchrotron) for durability.” And how did additive manufacturing speed up this work? “Metal 3D printing removed tooling constraints, enabling rapid, low-risk design iterations and precise internal geometries that conventional manufacturing cannot produce, accelerating prototyping while delivering step-change performance without rearchitecting the transmission,” confirms Fuller.
DEMAND-DRIVEN DEVELOPMENT
Having achieved such remarkable technical achievements does Fuller feel we have now reached the pinnacle of heat transfer technology for road cars? On the contrary, he says: “We’re just getting started! As the industry pivots to hybrids, mainstream demand for compact intercoolers, oil coolers and power electronics thermal hardware is increasing and manufacturers are seeking solutions where tooling free iteration wins on
both performance and time to market. “With structural cost declines happening in metal AM, our F1grade cooling technology becomes accessible to general automotive in the near future, especially as OEM hybridisation and higher under bonnet heat loads intensify. The next evolution couples thinner, pressure capable walls and finer fin features with AI assisted CFD. We’re actively compressing our design test loops and scaling our capabilities to support volume production,” he details. As well as growing the automotive side of his business, Fuller is also focusing on the increasing demand for his solutions from other sectors. He explains: “We already support aerospace, defence and industrial applications where heat flux and footprint constraints are extreme. The biggest bottlenecks are showing up where power density and packaging collide, such as data centres/server racks, EV power electronics and batteries, hydrogen/fuel cell and avionics cooling, and compact industrial systems. Conventional heat exchangers hit limits on pressure drop, size and supplier responsiveness. That’s why enquiries keep arriving from every direction; the heat exchange problem is ubiquitous, so we prioritise focus, helping all customers meet higher heat rejection targets in tighter envelopes while maintaining a clear path from prototype to series production.“ Fuller is exploring a number of options as part of Conflux’s own scaling journey, including licensing some of its technology. “Conflux Production Systems (CPS), our manufacturing model for additively manufactured heat exchangers, will be available to our customers as a licensing option. Select partners can deploy a CPS line within their own facilities under our qualification, process controls, and QA/cleanliness regimes to scale production closer to final assembly,” he explains. “We remain open to strategic co development and long term supply across automotive, motorsport, aerospace, space, defence, and industrial sectors, using CPS licensing where it accelerates adoption, de risks logistics, and supports distributed, compliant manufacturing,” he adds.
www.engineerlive.com
7
AUTOMOTIVE DESIGN
A SOLID APPROACH Solid-state battery design enters an inflection point as the race towards commercialisation hots up
A
fter years of declining sales, shrinking margins, and a major corporate restructuring, Nissan is pushing to re-establish itself as a technological leader. While the carmaker’s recovery plan includes plant closures, layoffs, and a refreshed product portfolio, its R&D organisation has not slowed. In the background of a difficult transition, Nissan has quietly positioned itself at the forefront of one of the most consequential energy-storage shifts of the decade: the industrialisation of solid-state batteries (SSBs). According to recent reporting, Nissan’s prototype all-solid-state cells have now reached performance levels suitable for mass production, with support from Sacramento-based LiCAP Technologies. LiCAP specialises in dry-electrode fabrication, a manufacturing method that eliminates
solvent-based slurry coating - a breakthrough many industry analysts view as essential for economically viable solid-state production. Combined with Nissan’s ASSB pilot line, operating since early 2025, the company is targeting pack-level costs of around $75/kWh, far below last year’s global average of $115/kWh. These developments align with broader industry trends identified in IDTechEx’s Solid-State Batteries 2026–2036 analysis, which forecasts a US$10 billion SSB market by 2036 driven by automotive demand, materials innovation, and regionalised supply-chain strategies.
DRY ELECTRODE PROCESSING
The introduction of dry electrodes is arguably the most strategically significant element of Nissan’s SSB development. The conventional wet
Comparison of solid-state batteries by IDTechEx
8
www.engineerlive.com
process requires the mixing of active materials, conductive additives, and binders into a solvent slurry before coating, drying, and calendaring. This adds energy cost, time, and large capital expenditure for long drying ovens. Dry-electrode processing, by contrast, compacts a dry powder mixture directly onto the current collector using roll-pressing equipment. The absence of solvent significantly reduces energy consumption and removes the bottleneck of oven drying – a major impediment to both cost reduction and gigawatt-scale throughput. However, executing dry-electrode manufacturing at high uniformity and low defect rates is exceptionally challenging. Nissan’s partnership with LiCAP – already operating a 300 MWh production line for its Activated Dry Electrode process – suggests the automaker is accelerating toward
AUTOMOTIVE DESIGN
manufacturable, large-format cells more rapidly than many competitors.
GLOBAL COMPETITION INTENSIFIES
Nissan is not alone in pushing toward commercial-scale SSBs. In recent months, QuantumScape, backed by Volkswagen, began shipping near-production SSB samples to customers, while Factorial Energy in Massachusetts is currently preparing joint test programmes with Mercedes-Benz and Stellantis. South Korea, Japan, and China continue to dominate materials and electrolyte innovation, while the US and Europe invest heavily in localisation to reduce dependence on East Asia. This reflects the global dynamics outlined by IDTechEx: SSB progress now hinges on integrated ecosystems – materials suppliers, gigafactories, OEMs, and advanced manufacturing start-ups – rather than cell developers operating in isolation.
Nissan’s Hyper Force concept vehicle features an all-electric powertrain with a solid-state battery
instead, manufacturers are adopting hybrid solid–semi-solid approaches to improve manufacturability and reduce stack pressure requirements.
THE HURDLE BETWEEN LAB AND MARKET MATURING ELECTROLYTE SYSTEMS While laboratory cells routinely Solid-state batteries replace flammable organic liquids with solid electrolytes, improving safety and enabling highcapacity lithium-metal anodes. But each electrolyte system presents distinct engineering trade-offs: Sulfide Electrolytes • High ionic conductivity (~10-² S/cm) •C ompatible with cold-pressing and scalable powder processing • Air-sensitive, generating H2S and requiring stringent moisture control Oxide (Garnet) Electrolytes • Outstanding chemical stability with lithium metal • Require high-temperature sintering and face contact-resistance challenges • Well-suited for long-life stationary storage Polymer Electrolytes • Highly manufacturable and flexible • Limited room-temperature conductivity • Emerging block-copolymer and ceramic-filled variants mitigate dendrite formation As the IDTechEx report highlights, no single technology is dominant;
demonstrate high energy density and safety, mass production remains the principal barrier to commercialisation. Key engineering challenges include: • Achieving high-density interfaces between electrolyte and electrode without liquid infiltration • Suppressing lithium dendrites in solid–solid contact systems, especially under fast charge • Maintaining stack pressure uniformly across large pouch cells • Tight particle-size control for powder-based electrolytes to avoid porosity-driven impedance • Developing gigascale dry-room conditions, particularly for moisture-sensitive sulfides Nissan’s pilot line confirms that OEMs are transitioning from cell-level optimisation to systemlevel engineering, including pack integration, mechanical design, thermal management, and advanced battery management strategies tailored to solid-state chemistries.
PERFORMANCE AND COST OUTLOOK
If Nissan achieves its cost target of $75/kWh, solid-state batteries could undercut current lithium-ion packs
while delivering: • ~2× energy density, enabling 600–800 km EV ranges • One-third charging time, through high-rate lithium-metal architectures • Improved safety, thanks to nonflammable electrolytes and stable thermal behaviour • Reduced pack size and mass, benefitting vehicle architecture and efficiency IDTechEx forecasts that the first wave of SSB adoption will occur in premium EVs, heavy-duty trucks, UAVs, and defence applications, followed by cost-down diffusion into mass-market passenger cars in the early 2030s.
BETTING ON SOLID-STATE
Nissan’s resurgence may be uncertain, but its solid-state battery progress signals a broader shift: SSBs are moving from decade-long promise to tangible industrial development. With the convergence of dry-electrode manufacturing, maturing sulfide chemistries, and aggressive global investment, the industry is entering a critical inflection point. For engineers, the story is no longer whether solid-state batteries will arrive, but how quickly companies like Nissan, QuantumScape, Factorial, Toyota, and emerging US start-ups can overcome the last engineering barriers standing between pilot lines and true gigafactory-scale production.
www.engineerlive.com
9
ADDITIVE MANUFACTURING
EOS M4 ONYX POWER IN EVERY BUILD.
Metal 3D printing that enables high-volume production, secures long-term reliability and opens up new applications across industries.
Watch our webinar now and get all insights!
AI-Powered Automated Quality Inspection • Uses deep learning for high accuracy in complex, variable environments.
Meat & Protein
Fruit & Vegetable
Building Materials
Medical
Packaging
Weld
Medical catheter defect detection
• Highly adaptable, learning from new data to enhance performance. • Thrives in uncertain environments, handling high variability. • Scalable with no significant resource increase as production grows.
Learn more about FactorySmart AI
10
www.engineerlive.com
visit lmi3D.com/IDE-AI
ADDITIVE MANUFACTURING
ADAPTIVE TWISTING METAMATERIALS 3D printed breakthrough for next-generation vehicle crash protection
A
collaborative research team from the University of Glasgow, the Polytechnic University of Marche, the University of L’Aquila and Italy’s National Institute for Nuclear Physics has developed a new class of 3D-printed metamaterials that could redefine how vehicles manage impact energy. Published in Advanced Materials, the work introduces adaptive twisting metamaterials - architected steel structures whose mechanical response can be tuned to different crash scenarios without electronics, hydraulics, or active controls. At the core of the innovation is a gyroid lattice architecture produced through metal additive manufacturing. Gyroid-based structures have long been of interest for their ultra-low density and high strength-to-weight ratio, but the researchers have exploited a unique characteristic: when compressed, the lattice can convert axial strain into a corkscrew-like rotational deformation. This twist provides a new degree of freedom in crash-energy management, enabling programmable stiffness and energy absorption.
PROGRAMMABLE ENERGY ABSORPTION
Conventional crash-mitigation systems such as aluminium crumple zones and polymer foams are inherently static. They are designed for a specific load case and typically cannot adapt to variations in impact direction, magnitude, or rate. Professor Shanmugam Kumar of the University of Glasgow, who led the research, notes that, “the protective materials used in most vehicles today are static, designed for specific impact scenarios and unable to adapt to varying conditions.” The team instead demonstrated that rotation constraints applied at the boundaries of the gyroid material
Influence of torque ratio on the torque directions, rotations, and torsional loading configurations of CCW twisting metamaterial (righthanded micropolar metamaterial)
allow engineers to mechanically tune its behaviour. Three configurations were tested under both dynamic impacts and quasi-static loading: • Fully constrained (no twist): Maximum stiffness, absorbing 15.36 J/g of energy – the highest of all configurations • Freely twisting: Approximately 10% reduction in stiffness and absorption, resulting in a softer, more compliant response • Over-twisted (forced rotation): A 33% reduction in absorption, illustrating the tunability range This spectrum, from rigid shielding to compliant cushioning, could enable a single material system to replace today’s mix of crash structures designed for different load cases.
ADVANCED MODELLING AND MANUFACTURING INTEGRATION
To support the experimental work, the researchers developed a computational model capable of predicting gyroid-twist behaviour across strain rates. Importantly, they incorporated real-world manufacturing imperfections into the model by reconstructing the printed lattices using micro-CT scanning. This alignment between numerical and experimental results is critical for validating metamaterial architectures intended for safetycritical applications. The material is fabricated entirely from steel using additive manufacturing, allowing the precise control needed to generate gyroid lattices with the required porosity and geometric continuity. AM also enables local modifications such as variable pore size or lattice density, opening additional design degrees of freedom for engineers seeking to tailor response zones within vehicle structures.
IMPLICATIONS FOR AUTOMOTIVE ENGINEERING
The potential applications extend far beyond a simple structural insert. Because the gyroid can convert linear impact loads into rotational motion, the material opens new possibilities for rotational-energy absorbers, hybrid crash-mitigation systems and even mechanical impact-energy harvesters. Professor Kumar notes that the metamaterial “could find applications in both automotive and aerospace safety… and could also support the development of novel forms of energy harvesting, by converting impacts into rotational kinetic energy.” For vehicle manufacturers, the concept aligns with a growing trend toward multifunctional crash structures that offer improved performance without increased weight or complexity. The tunable nature of the material may also reduce the need for complex active safety actuators that must withstand milliseconds-scale loads.
ADAPTIVE, ELECTRONICS-FREE SAFETY SYSTEMS
While still in early development, adaptive twisting metamaterials present a compelling new direction for passive safety engineering. They demonstrate that adaptability can be achieved through architected materials alone, reducing system complexity while offering engineers a new design parameter: rotational freedom. As regulatory pressures and realworld crash variability continue to grow, architected materials that can dynamically adjust to impact severity may become a cornerstone of nextgeneration automotive and aerospace protection systems.
www.engineerlive.com
11
ADDITIVE MANUFACTURING
The EOS M4 ONYX metal 3D printer
BREAKING
MANUFACTURING BARRIERS
M
Sebastian Becker explains how metal 3D printing is powering scalable production
anufacturing is undergoing one of the most significant shifts in decades. Companies face growing pressure to deliver complex parts faster, at lower cost, and with greater sustainability. Traditional processes often stand in the way - high tooling expenses, long setup times, and rigid workflows slow innovation and make scaling difficult. What’s different today? The value of industrial 3D printing is no longer up for debate. Instead, the question has shifted: How can additive manufacturing (AM) scale efficiently - delivering more lasers per square metre to meet the growing demand for serial AM parts?
we are ready to deliver large scale serial production (3 shifts, 24/7, 97% uptime) This shift requires lowest cost per part, certified repeatability, high throughput, automation readiness, and seamless integration into digital factory ecosystems. Yet many AM systems still struggle with insufficient build rates, low uptime, manual job handling, and high consumable usage factors that can turn AM into a
bottleneck instead of an enabler. Manufacturers increasingly need platforms specifically engineered for continuous, scalable output, including automation to maximise uptime.
CUSTOMER FOCUS: SCALING AM WITH REAL IMPACT
KSB, a global leader in pump and valve solutions, produces a complex particle separator for removing solids
THE MARKET REALITY
AM has dipped its toes into small and medium scale production (think hip cups or satellite parts), and with the development of the EOS M4 ONYX
12
www.engineerlive.com
Industrial metal 3D printing is driving the shift toward scalable, digital manufacturing
ADDITIVE MANUFACTURING
Particle separator from KSB printed on the EOS M4 ONYX
from liquids - a critical component for pump performance and longevity. KSB engineered this as a true AM part, only buildable with metal industrial 3D printing. Once design constraints were overcome, the next challenge was scaling production to meet cost-per-part targets. Seeking higher productivity and lower operational costs, KSB introduced and built the component on an industrial metal AM platform by EOS, achieving the following results: • Powder utilisation: 80% sintered into the part, 19% recyclable, only 1% waste EOS’ RFS PRO next-gen recirculation filter system
• Productivity: Increased by more than 60% thanks to 97% system uptime and less than 30-minute job changeover • Build time per part: Reduced by over 40% • Cycle Details: 55 hours total build time The key to this success was the combination of a large 450 × 450 × 400mm build volume with highperformance multi-laser technology, enabling up to 50% higher throughput. Smart Fusion optimises exposure strategies to minimise rework and
reduce cost per part. Automated job changeovers minimise downtime, while the RFS Pro filter system cutting hazardous waste by up to 90% - strengthens sustainability. Together, these elements deliver measurable gains in efficiency, cost performance, and environmental responsibility.
A NEW ERA FOR INDUSTRIAL AM
As industries accelerate their digital transformation, scalable metal AM has become an essential part of competitive manufacturing. By moving beyond the limits of traditional processes and adopting next generation AM systems, companies can increase productivity, flexibility, and sustainability today. The KSB case demonstrates how businesses are evolving from limited output to reliable, industrial scale AM with clear, quantifiable results. Powered by multi-laser capability, intelligent software, and automated workflows, metal AM has fully arrived in industrial production delivering real performance and competitiveness now.
Sebastian Becker is head of product management metal at EOS. www.eos.info/metal-solutions
www.engineerlive.com
13
SPECIAL FEATURE DIGITAL TWINS
A NEW ERA FOR
SIMULATION
Digital twins enable faster and more cost-effective simulation, testing, and optimisation
Lydia Arundel explores how Siemens’ acquisition of Altair has boosted its industrial software portfolio, enabling faster innovation through advanced simulation and AI
I
n March 2025, Siemens completed its acquisition of Altair Engineering, a provider of software for industrial simulation and analysis, enabling Siemens to add new capabilities in mechanical and electromagnetic simulation, highperformance computing (HPC), data science, and AI. The acquisition of Altair and its technology enables Siemens to further advance the most comprehensive digital twin, making simulation more accessible to companies of any size so they can bring their products to market faster. “We welcome the Altair community of customers, partners and colleagues to Siemens. Adding Altair’s groundbreaking innovations to the Siemens Xcelerator platform will create the world’s most complete AI-powered design, engineering and simulation portfolio. Together, we will help our customers to innovate at the scale and speed that today’s complexity-driven world demands,”
14
www.engineerlive.com
says Roland Busch, president and CEO of Siemens AG. “Through the ONE Tech Company programme, we will extend our leadership in industrial software. This enables all industries to benefit from the revolution driven by data and AI.” Integrating Altair’s capabilities in simulation, HPC, data science, and AI enables Siemens customers to access new simulation expertise, optimise HPC processes, develop new AI tools, and perform data analytics to support innovation and digital transformation for companies of any size. Peter De Clerck, global head of product marketing, simulation, data analytics, and HPC at Siemens Digital Industries Software, described the acquisition as less about the additional tools and more about closing gaps across the engineering lifecycle. De Clerck explains, “Altair is bringing mainly three big components. Expanded capabilities in simulation (HyperWorks), data analytics and AI capabilities
(Rapidminer), and software to manage large supercomputers and cloud computing (HPCWorks).” It is these additions that strengthen Siemens’ engineering ecosystem, from early concept simulations to digital twins.
THE DIGITAL TWIN AND THE DIGITAL THREAD
The Digital Twin has become a significant principle of Siemens’ long-term vision, De Clerck says, “To be successful as a development organisation in the future, you need to have a digital twin, really a complete digital replica of what you intend to build.” A comprehensive digital twin enables simulation, testing, and optimisation to be faster and more cost-effective in comparison to a physical prototype. Siemens also believes the digital thread, the seamless movement of engineering data and knowledge across the entire
Peter De Clerck, global head of marketing, simulation, data analytics, and HPC at Siemens Digital Industries Software
lifecycle, is equally important. “If you want to create efficiency, it’s crucial to have continuous information throughout the development cycle, production, and even usage,” De Clerck explains. Teamcenter forms the backbone of this connectivity, anchoring simulations, CAD models, requirements and manufacturing data in a single context-rich environment. The AI age has made it even more critical that engineering data is unified; it is the digital thread that has the potential to enable trustworthy, scalable AI for engineering. As De Clerck states, “If you want to use data to train an AI model, you need to provide the context of how that model was built.” Altair’s portfolio enhances Siemens’ coverage in various areas, including:
SPECIAL FEATURE DIGITAL TWINS
If you want to use data to train an AI model, you need to provide the context of how that model was built
ELECTROMAGNETICS
Electromagnetics is potentially the most significant and most commercially relevant new addition from a physics perpective. De Clerck explains, “Electromagnetics was a big gap we had. Altair closes that gap with high-frequency EM for radar and antenna applications, and lowfrequency EM for electric motors.” As products become more connected and electrified, these simulations are no longer optional; they become central to the design of vehicles, consumer electronics, smart infrastructure, and industrial systems.
STRUCTURAL NON-LINEARITIES AND CRASH SIMULATION
Altair’s Radioss solver provides advanced non-linear deformation capabilities for crash, drop, and impact, which are vital for automotive, aerospace, defence, and consumer product markets.
DISCRETE ELEMENT MODELLING
Discrete element modelling (DEM) is used to simulate granular and bulk materials, an approach that is becoming increasingly important in manufacturing. DEM is utilised by sectors such as battery manufacturing, food processing, and pharmaceuticals.
FROM CONCEPT TO IN-USE OPERATION
Physical testing digital twins with Simcenter TestLab and Simcenter 3D
The combined portfolio supports every phase of product development, which is categorised into six stages: • Concept design • Designer-level simulation • Detailed engineering • Physical testing • Manufacturing simulation • In-operation digital twins
A GAME-CHANGER FOR ENGINEERING
The acquisition offers several benefits for customers, but none more so than AI-powered simulation: “What’s happening with AI is fundamentally changing engineering. It speeds things up drastically and unlocks design spaces people would never have thought about.”
When neural networks are integrated into simulation processes, engineers can run physics-based simulations to generate training data, then utilise AI to predict outcomes almost instantaneously during design exploration, significantly reducing compute time. Speed is the primary benefit: “Simulation used to be too slow to influence design. Now it can.” Faster simulation leads to either shorter time-to-market or more opportunities to improve a product before launch. As De Clerck says, “Driving productivity is as important as empowering innovation.” Together, Siemens and Altair enable faster innovation through unified simulation, AI, and Digital Twin technology.
www.engineerlive.com
15
INSTRUMENTATION & ELECTRONICS
Atlascan Pro features intuitive workflows, guided software and quick-start training kits
HANDHELD IN HIGH-FIDELITY Introducing Hexagon’s latest advancement in handheld metrology for accessible high-fidelity 3D capture
T
he rapid evolution of handheld 3D scanning technology is reshaping the landscape of industrial metrology, reverse engineering, and digital manufacturing. Once dominated by high-end laser trackers and fixed CMMs capable of submicron precision but often limited in flexibility, the portable scanning market has now emerged as a credible counterpart, capable of delivering dense point clouds, high repeatability, and workflow integration once considered the exclusive territory of laboratory-grade systems. Hexagon Manufacturing Intelligence
16
www.engineerlive.com
has been at the forefront of highprecision measurement for decades, with its flagship Leica Absolute Tracker and AS1 scanner widely used in elite motorsport, aerospace assembly and quality-critical production environments. As Robin Wolstenholme, global media relations and analyst relations manager of Hexagon’s Manufacturing Intelligence division puts it, “we’re really, really well known for the high-end stuff, such as the high-precision laser trackers Red Bull use day in, day out to measure a single line of paint.” But as demand for accessible metrology grows - particularly for
reverse engineering, large-volume inspection and real-world, in-situ measurements - Hexagon has broadened its portfolio. The company has moved decisively into robust, affordable handheld scanning tools designed for engineering teams who “still need something trustworthy and metrology grade, but don’t necessarily need 12-micron precision or want to measure everything from 15 metres away.” This strategy has culminated in the launch of the Atlascan Pro, a new handheld scanner that bridges the gap between consumer-grade 3D scanning and high-end industrial metrology,
INSTRUMENTATION & ELECTRONICS
while maintaining the reliability and data quality expected from a metrology company.
PORTABLE METROLOGY Hexagon’s shift toward handheld scanners began with the MarvelScan, a wireless, highly portable scanner designed for heavy engineering, MRO and hard-to-reach inspection environments. “A lot of customers in the UK are making submarines, big gearboxes, things with inspection hatches,” Wolstenholme explains. “Things that require someone having to crawl inside, and that are hard to measure.” The ability to bring the scanner to the part – not the part to the measurement system – has made handhelds indispensable for a wide range of applications, from truck, bus and heavy equipment manufacturing to oil and gas inspection and reverse engineering legacy parts. Handheld systems also eliminate much of the infrastructure required for largevolume measurement. “You don’t necessarily need a laser tracker for everything,” Wolstenholme says. “These are devices that can just go in and scan stuff – incredibly powerful, super portable, with a lot of on-device control.”
DYNAMIC TRACKING AT SCALE
To cover even larger components, Hexagon introduced HyperScan, a dynamically tracked scanning system using external optical cameras. Instead of relying solely on stickers and
Atlascan Pro is designed to make handheld scanning attainable for SMEs, R&D teams and educators
onboard cameras, HyperScan separates the tracking and scanning functions, enabling metrology-grade tracking over volumes up to six metres. “We take the cameras out of the scanner, put them on a camera bar, and the scanner gets tracked dynamically,” Wolstenholme explains. “It’s a cost-effective way of going around and measuring things like cars, cabs of trucks, oil and gas equipment – anything large.” For automation, these scanners integrate into Hexagon’s PRESTO robotic inspection platform. A PRESTO cell built from HyperScan components can achieve large-volume automated inspection at dramatically lower cost than a laser-tracker-based cell. This is critical for automotive suppliers, MRO centres and mid-tier manufacturers seeking to adopt nearOEM-level inspection capability. “You start to be able to take truly automated inspection down the supply chain,” he adds.
INTRODUCING THE ATLASCAN PRO
The latest addition to the portfolio, the Atlascan Pro, represents a significant strategic shift. While Hexagon’s previous handhelds were metrologygrade systems designed with inspection accuracy as the priority, the Atlascan Pro is specifically optimised for reverse engineering, featuring high-resolution surface capture, rapid point cloud generation and integration with CAD and design software. “What we’ve done is create a product that is still incredibly robust, with
REAL-WORLD APPLICATIONS The flexibility of handheld scanners makes them suitable for a wide range of unconventional environments. As application engineers note, these systems have been used on: • Bridges • Fireplaces • Car seats and interiors • Boats, trains and aircraft • Drainage infrastructure • Pelton wheels in hydroelectric stations WOLSTENHOLME HIGHLIGHTS ONE NOTABLE EXAMPLE: “There was a Pelton wheel in the French Alps – a big hydroelectric installation. The wheel was broken, and we reverse-engineered it. The scanner matters – the data has to be trustworthy.” In shipbuilding and defence, engineers frequently work in constrained, vibration-prone environments. “You could be up inside a submarine measuring structures with millimetre tolerances,” he says. “The ability to pick up the scanner and just get a clean, accurate scan – that’s critical.” Target-based tracking allows handheld scanners to compensate for movement, vibration, or unstable mounting surfaces. This makes them uniquely suited to on-site, fullscale industrial measurement.
www.engineerlive.com
17
INSTRUMENTATION & ELECTRONICS
very high point density and resolution – up to eight million points per second – but also very cost-effective,” says Wolstenholme. “So literally any machine shop or engineering department could buy one.” Key technical features include: • Dual-mode laser line arrays for fast coverage and fine feature capture • Up to 8 million points per second • High-density point clouds suitable for reverse engineering and CAD reconstruction • Ergonomic, portable design for field use • Optimised workflow for handheld scanning Although Hexagon does not classify the scanner as “metrology grade” due to its strict internal standards, Wolstenholme is clear: “It’s low precision only relative to the very highest-precision systems. Of course you can use it for quality control. The data is incredibly clean.”
CLOSING THE LOOP
One of the most significant elements of the Atlascan Pro offering is software integration. Hexagon now owns Geomagic Design X, the world’s leading reverse engineering platform. As Wolstenholme puts it, “we are effectively giving away Design X with the scanner – the best reverse engineering software on the planet. You can scan straight into Design X, hit a button, and reverse engineer directly into CAD.” This creates an end-to-end workflow where the user captures the part with the Atlascan Pro, point cloud data is
Operators can capture accurate data without complex setup or specialist training
18
www.engineerlive.com
Atlascan Pro boasts a lightweight, ergonomic design
streamed directly into Design X, and CAD surfaces are generated semiautomatically. Models can then be exported to Creo, SolidWorks, NX and other platforms via dedicated plugins. For engineering teams working with legacy components, discontinued parts or prototype development, this is transformative. “Whether you’re reverse-engineering a plastic toy, a bumper, a metal widget or a legacy aerospace component,” Wolstenholme explains, “you want a high-quality point cloud so you don’t miss data, and so you spend as little time as possible turning it back into CAD.”
A MORE DEMOCRATIC FUTURE
What emerges from Hexagon’s handheld scanning strategy is a deliberate attempt to democratise high-quality measurement tools. Rather
than confining advanced scanning to OEM-level facilities, Hexagon is pushing capabilities down to smaller engineering teams, independent machine shops, MRO providers and even aftermarket specialists. “It’s the people who matter,” Wolstenholme emphasises. “There’s no enterprise here – it’s users. If you’re an engineer who knows CAD, you’ll find Design X and these scanners very easy to pick up.” By maintaining core metrology principles – data integrity, repeatability, calibration, traceability – while lowering the cost and skill barriers to adoption, Hexagon is enabling a broader engineering base to participate in digital manufacturing workflows long dominated by major OEMs.
THE CONTINUED RISE OF PORTABLE SCANNING
Portable 3D scanning has matured from convenience tool to core engineering instrument. High-density point clouds, CAD-native workflows and robust, fieldready hardware now make handheld scanners viable for everything from reverse engineering and prototyping to inspection and large-volume production support. And with Hexagon’s strategy of accessibility and reliability, handheld scanning appears poised for widespread adoption across engineering disciplines. As Wolstenholme concludes, “We’ve built something incredibly dependable, very easy to use, and affordable. You just pick it up, scan, and go straight into CAD. It’s exactly what a lot of our customers have been asking for.”
INSTRUMENTATION & ELECTRONICS
Linear Motion Specialists
Authorised NSK & Nippon Bearing Distributor
RM Fowler Ltd High precision linear guides and ball screws NSK K1 lubricating units to extend maintenance intervals NH series available with high temperature design RA roller guides for high load, rigidity and precision PU/PE Miniature series with high corrosion resistance Precision cross roller non-recirculating slide ways Slide bush, Topball, Stroke bush and Ball splines Precision curved cross roller Gonio Ways
01565 651 051 sales@rmfowler.co.uk
www.rmfowler.co.uk
www.engineerlive.com
19
INSTRUMENTATION & ELECTRONICS
COMING OF AGE How generative design is reshaping engineering workflows
Demonstrating project Bernini
G
enerative design has moved rapidly from an experimental capability to a core engineering tool, driven by advances in artificial intelligence, machine learning and cloud-native platforms. Recent announcements from Dassault Systèmes, Autodesk and Siemens highlight how generative approaches are now being embedded across mechanical CAD, manufacturing, and electronic design automation (EDA), fundamentally changing how engineers create, evaluate and optimise designs.
While early generative design tools focused on topology optimisation or automated concept generation, the latest developments point to a broader transformation: AI systems that actively participate in engineering workflows, generate editable geometry, automate verification, and integrate design intent across disciplines.
GENERATIVE AI ENTERS MAINSTREAM CAD Dassault Systèmes’ release of Solidworks 2026 marks a significant step in normalising generative AI
Solidworks delivers new features and performance upgrades every 10 weeks
20
www.engineerlive.com
within everyday mechanical design workflows. Rather than positioning generative design as a specialist function, the new release embeds AI directly into drawing creation, detailing and assembly modelling. A notable enhancement is AIassisted assembly creation, where the system automatically recognises components that resemble standard fasteners – such as bolts, nuts and washers – and assembles them accordingly. This capability reduces manual modelling effort, improves consistency, and minimises common assembly errors, particularly in large mechanical systems. Generative AI is also being applied to drawing creation, accelerating detailing and documentation while improving traceability. By automating repetitive drafting tasks and linking changes directly to evaluated attributes, Solidworks 2026 supports more robust change management, an area where manual processes have traditionally introduced risk. Beyond geometry, Dassault has introduced an AI-powered virtual companion designed to extract and summarise engineering knowledge from community forums, wikis and
INSTRUMENTATION & ELECTRONICS
internal documentation. For design engineers working under schedule pressure, this represents a shift toward context-aware assistance embedded directly in the design environment, reducing the friction between problem identification and resolution. Although these features may appear incremental, they reflect a broader trend: generative AI is being used not just to create new forms, but to compress design cycles, reduce cognitive load and improve collaboration across distributed engineering teams.
FROM TEXT PROMPT TO EDITABLE GEOMETRY If Solidworks 2026 represents generative AI augmentation, Autodesk’s announcements at Autodesk University 2025 (AU2025) signal a more radical rethinking of CAD itself. Autodesk has been investing heavily in AI across its three industry clouds – Forma (construction), Flow (entertainment) and Fusion (manufacturing) – with generative capabilities native to each platform. The most disruptive development is Autodesk’s work on Neural CAD, an AI foundation model capable of generating fully editable CAD geometry from a single text prompt. Built on Autodesk’s proprietary manufacturingfocused models and originating from the company’s Project Bernini research (covered in our April 2025 issue), this approach moves beyond generative suggestions to true geometry creation within the CAD kernel. Unlike earlier generative design tools that produced optimisation outputs requiring reinterpretation, Neural CAD aims to deliver parametric, editable models that engineers can immediately refine. In demonstrations, Autodesk showed how a simple prompt could generate a baseline air fryer design, which could then be modified using standard CAD operations. For professional engineers, the implication is significant: concept generation, traditionally a timeintensive and experience-driven phase, could be accelerated dramatically. However, Autodesk has emphasised that engineers remain “in the loop,” acting as evaluators and decisionmakers rather than passive recipients
A water pitcher generated on Autodesk’s Bernini AI model
of AI-generated designs. The intent is not to replace engineering judgement, but to expand the design space and lower barriers to participation. Autodesk has also focused on practical integration. Fusion’s generative capabilities connect directly to manufacturing toolpaths, PLM workflows and even external platforms such as Microsoft 365, enabling downstream reuse of design data for visualisation, documentation and communication.
requirements are increasingly difficult to manage using traditional methods. The deployment of AI-powered Solido workflows across major foundries underscores a key point: generative design is as much about verification and optimisation as it is about geometry creation. In safetycritical sectors such as automotive, aerospace and industrial electronics, AI is being used to increase confidence and reduce time-to-qualification without compromising reliability.
GENERATIVE DESIGN BEYOND MECHANICS
COMMON THEMES
In electronic design automation, meanwhile, Siemens’ Solido software illustrates how AI-driven optimisation is becoming critical for advanced semiconductor design, particularly in analogue, RF and reliability-critical applications. Certus Semiconductor’s adoption of Solido for IO and ESD library development highlights a parallel evolution in EDA. Instead of manually iterating across thousands of process, voltage and temperature corners, Solido applies machine learning to accelerate design space exploration, variation-aware verification and IP characterisation. For analogue and mixed-signal engineers, this represents a generative approach at the circuit level: AI models predict performance trends, identify corner-case failures and optimise designs while maintaining SPICE-level accuracy. This is especially relevant at advanced process nodes, where variability, reliability and compliance
Across mechanical CAD, manufacturing and EDA, several common themes emerge. First is the rise of domainspecific foundation models – AI systems trained not just on generic data, but on engineering-specific representations, constraints and physics. This specialisation is critical for reducing errors and ensuring outputs remain physically and functionally meaningful. Second is the emphasis on IP protection. Autodesk, for example, has highlighted safeguards that discard generated outputs resembling training data, ensuring customer IP is not inadvertently reproduced. As generative design becomes more pervasive, trust in data governance will be essential for adoption in commercial engineering environments. Finally, all three companies stress the continued role of the engineer. Whether through editable Neural CAD models, AI-assisted drafting or ML-driven circuit verification, generative tools are positioned as collaborators rather than autonomous designers.
www.engineerlive.com
21
MATERIALS, PROCESSES, FINISHES
Dr Ben Hargreaves, sales area manager – UK & Ireland at Lati UK
ALUMINIUM ALTERNATIVE Lati’s Ben Hargreaves explains how thermally conductive plastics can offer a more sustainable and performance-optimised choice over aluminium
T
hermal management remains one of the defining engineering challenges across sectors ranging from LED lighting and power electronics to electric vehicles and industrial motors. As power densities rise and packaging volumes shrink, engineers are under pressure to dissipate heat efficiently while also addressing cost, manufacturability and environmental performance. Against this backdrop, thermally conductive plastics are increasingly being evaluated as alternatives to traditional die-cast aluminium solutions. According to Dr Ben Hargreaves, sales area manager – UK & Ireland at Lati UK, advances in polymer compounding, certification and lifecycle assessment are enabling these materials to move beyond niche applications and into mainstream
22
www.engineerlive.com
engineering use. “We spend a huge amount of time, effort and investment ensuring our materials meet demanding regulatory standards,” he explained during a presentation at the recent Advanced Engineering exhibition in Birmingham, UK. “Across our portfolio we have around 50 grades with active UL Yellow Cards, alongside rail certification and other sector-specific approvals.”
MATERIAL PLATFORMS AND FILLERS
At a fundamental level, thermally conductive plastics are created by combining a polymer matrix with thermally conductive fillers. While the underlying concept is straightforward, the execution is highly specialised. “In very simple terms, we take a polymer, add a thermally conductive filler, and that gives us our compound,” says
Hargreaves. “In practice, there is a great deal of know-how required to balance thermal, mechanical and processing performance.” The fillers typically fall into two categories: graphite-based and ceramic-based. Graphite fillers enable the highest thermal conductivities achievable in polymers, reaching values of up to around 30W/m·K. However, graphite also introduces electrical conductivity, which can be unacceptable in certain applications. Ceramic fillers, by contrast, offer electrical insulation but lower thermal conductivity, typically in the high single digits up to around 10W/m·K. “Graphite-filled compounds give you the best thermal performance, but you have to accept some electrical conductivity,” Hargreaves noted. “Ceramic-filled systems won’t get you to the same conductivity levels,
MATERIALS, PROCESSES, FINISHES
Lati offers a wide range of structural engineering polymers
but they are electrically insulating, colourable, and non-marking, which can be critical in many electrical and electronic applications.” Both material families can retain good mechanical properties, dimensional stability and processability, including mouldability, machining and welding. Flameretardant variants are also available, particularly for ceramic-filled systems.
ANISOTROPHY AND DESIGN IMPLICATIONS
One of the key differences between thermally conductive plastics and metals lies in anisotropy. Aluminium is isotropic, meaning its thermal conductivity is the same in all directions. Filled polymers, particularly those using high aspect ratio fillers such as graphite or hexagonal boron nitride, exhibit direction-dependent conductivity due to filler alignment during injection moulding. “You tend to get much higher in-plane thermal conductivity than through-plane,” explained Hargreaves. “That’s not necessarily a problem, but it means you cannot take a ‘black metal’ approach and simply copy an aluminium design in plastic.” Instead, engineers must consider part geometry, gate locations, flow paths and rib or fin design to ensure heat is conducted away from sensitive components and dissipated effectively at the surface. Lati uses mould flow analysis combined with thermal simulation to predict filler orientation and heat dissipation performance before tooling is cut. “This allows us to give customers a very accurate picture of how the final part will behave thermally,” added Hargreaves.
RETHINKING HEAT DISSIPATION METRICS A common objection to thermally
Latiohm compounds are the company’s best-performing in terms of conductivity and mechanical resistance
conductive plastics is their lower conductivity compared with aluminium, which typically offers around 100W/m·K. However, Hargreaves argued that thermal conductivity alone is not the dominant factor in many real-world applications. “For the majority of natural convection applications, conductivity is not what determines how quickly heat is dissipated,” he says. “Once heat reaches the surface, convection is the critical mechanism.” Extensive testing, particularly in the lighting sector, has shown that plastics with thermal conductivity around 10W/m·K can perform comparably to aluminium heat sinks under natural convection conditions. Surface emissivity can also play a role, with matte, dark polymer surfaces sometimes offering better radiative heat transfer than shiny metal finishes. There are, of course, limits. Forced convection, very high heat fluxes or applications competing with low-cost extruded aluminium profiles remain areas where metals retain a clear advantage.
SUSTAINABILITY AND LIFECYCLE PERFORMANCE
Environmental performance is becoming an equally important selection criterion. “Sustainability is very, very important to us as a company,” said Hargreaves. “That’s why we’re increasingly offering materials with bio-based or recycled content that deliver exactly the same mechanical, thermal and fire performance as virgin grades.”
On a raw material basis, primary aluminium carries a global warming potential (GWP) of roughly 10kg CO2 per kilogram, while thermally conductive plastics can be significantly lower. Even when recycled aluminium is considered, a like-for-like comparison by mass is misleading due to density differences. “A more realistic comparison is GWP per part, not per kilo,” Hargreaves explains. “When you do that, thermally conductive plastics can show a clear advantage.” The benefits are amplified further by the use of chemically recycled polymers. Lati has demonstrated that switching from virgin nylon 6 to chemically recycled nylon 6 with identical filler content can roughly halve the GWP of the compound, even before accounting for processing, transport or end-of-life considerations.
ASSESSING THE APPLICATIONS
Typical applications include LED luminaires, electrical enclosures, power distribution components, motors and automotive electronics, particularly in electric vehicles where electrical insulation and weight reduction are critical. As devices become more compact and power densities increase, demand for materials that combine thermal performance, design freedom and sustainability is set to grow. “Thermally conductive plastics are not a universal replacement for aluminium,” Hargreaves concluded. “But in the right applications, with the right design approach, they can be cost-competitive, environmentally advantageous and technically robust.”
www.engineerlive.com
23
MATERIALS, PROCESSES, FINISHES
BEYOND LIMITS A high-voltage cathode breakthrough for next-generation batteries
Eder Lomeli, Edward Mu, and Hari Ramachandran (front row, from left) led an international team in getting an iron-based material to give up and take back five electrons. Image via Bill Rivard/Stanford University
E
ngineers working in energy storage have long regarded iron as an attractive but fundamentally limited cathode material. Abundant, lowcost and geopolitically secure, iron has already displaced cobalt and nickel in many lithium-ion batteries through lithium iron phosphate (LFP) chemistries. Yet iron’s relatively low operating voltage has constrained energy density, forcing designers to trade performance against sustainability and cost. New research led by Stanford University and SLAC National Accelerator Laboratory now challenges that assumption, demonstrating an iron-based cathode material capable of reversibly exchanging five electrons per iron atom - far beyond the two or three electrons previously thought possible. Published in Nature Materials, the work represents a significant advance in fundamental materials science with potentially wide-ranging engineering implications, from higherenergy lithium-ion batteries to future developments in magnetics and superconductivity.
BREAKING THE IRON CEILING
At the heart of the breakthrough is a long-standing question in redox chemistry: how many electrons can iron reliably donate and accept without destabilising its crystal structure? In most natural and engineered systems,
24
www.engineerlive.com
iron cycles between oxidation states involving two or three electrons. In his 2018 doctoral thesis, Stanford alumnus William Gent proposed that, under the right structural conditions, iron might be pushed to a much higher oxidation state, enabling significantly greater energy storage. Gent’s early work suggested a pathway but stopped short of a practical demonstration. That challenge was taken up several years later by Stanford PhD students Hari Ramachandran, Edward Mu and Eder Lomeli, who led a large interdisciplinary collaboration involving 23 researchers across universities and national laboratories in the US, Japan and South Korea. Their target was a lithium-ion battery cathode material composed of lithium, iron, antimony and oxygen, referred to as LFSO. The goal was to stabilise iron in an unusually highenergy redox state without triggering the side reactions that typically limit performance, such as oxygen loss or irreversible structural collapse.
ENGINEERING STABILITY AT THE NANOSCALE
Early attempts to realise Gent’s concept ran into a familiar problem for battery engineers: structural degradation during cycling. When lithium ions were extracted during charging, the cathode lattice distorted and collapsed, rendering the material unusable.
The solution turned out to be one of scale. By reducing the cathode particles to the nanoscale – around 300 to 400 nanometres in diameter, roughly 40 times smaller than previous iterations – the researchers were able to fundamentally change how the material responded to lithium extraction. “Making the particles that small was a significant challenge,” Ramachandran explains, but the team ultimately succeeded by growing the crystals from a carefully controlled liquid solution. Electrochemical testing suggested that the new material could indeed reversibly exchange five electrons per iron atom while maintaining structural integrity. To confirm the underlying mechanism, the team combined advanced spectroscopy with computational modelling. Detailed X-ray and neutron studies carried out at Lawrence Berkeley, Oak Ridge and Argonne national laboratories revealed that the additional redox capacity was not attributable to iron alone. Instead, oxygen atoms within the crystal lattice also participated in the charge compensation process, enabled by the specific geometric arrangement of the material. “The atoms in this very nicely arranged material behave like a single entity,” says Lomeli. This cooperative behaviour allows the system to reach a higher overall energy state than iron could achieve independently.
MATERIALS, PROCESSES, FINISHES
WHY VOLTAGE MATTERS
While LFP cathodes have become dominant – accounting for around 40% of lithium-ion batteries produced today – their lower voltage limits energy density at the pack level. “A high-voltage, iron-based cathode could avoid the trade-off between higher voltage and higher-cost metals that previously dominated cathode materials,” Mu notes. In principle, this would enable higher energy density without reverting to cobalt- or nickelrich chemistries that carry cost, ethical and supply-chain risks. Around 70% of global cobalt supply originates from the Democratic Republic of the Congo, where mining has been linked to environmental damage and unsafe labour practices. Nickel supply chains also face volatility as demand rises from both battery and stainless steel markets. Iron, by contrast, is plentiful, inexpensive and globally distributed.
DISCOVERY TO DEPLOYMENT
Despite their promise, significant
Previous attempts to force an iron-based cathode material to give up more electrons (top). Stanford/SLAC-led researchers’ new version (bottom) bends slightly to accommodate the retreating lithium and remains intact for its return
engineering work remains before LFSO-type materials could reach commercial use. While effective in stabilising the crystal structure, antimony is expensive and subject to its own supply constraints. The research team is now actively investigating alternative elements that could play a similar structural role without introducing new vulnerabilities. Other practical considerations include particle morphology, manufacturability at scale, long-term cycling stability and compatibility
with existing electrolyte systems. These are familiar hurdles for battery developers, but the underlying demonstration that iron can be pushed beyond a three-electron redox limit in a stable, reversible way represents a genuine step change. “Scientists have rarely reported high-voltage iron-based materials,” says project lead William Chueh. “Our detailed electronic structure exploration provides conclusive evidence of oxidation beyond three electrons.”
Surface Technologies l Controlled Shot Peening l Laser Peening l Keronite PEO l Thermal Spray Coatings l Dry Film Lubricants l Organic and Inorganic Coatings l Parylene Ultra-thin Conformal Coatings l Superfinishing l On-site Processing l Material Testing and Analysis l NADCAP, ISO 9001:2008, ISO 13485, AS9100 Rev D
www.cwst.co.uk • eurosales@cwst.com • 01635 279621 www.engineerlive.com
25
COMPOSITES
The implication for scalability is significant: fibre architecture can be created continuously, repeatably and with minimal labour input Sam Donegani, operations manager at Composite Braiding, speaking at Advanced Engineering in November 2025
SUSTAINABLE AT SCALE Composite Braiding’s Sam Donegani discusses high-volume composite braiding and circular design in structural applications
F
or all their well-documented advantages - high specific strength, stiffness and corrosion resistance – composites have historically struggled to achieve two things at once: true high-volume manufacture and credible sustainability. According to Sam Donegani, operations manager at Composite Braiding, those twin challenges are precisely why the company exists. “As a business, we really have two main reasons for being,” he explains. “High volume and sustainability in composites.”
UNLOCKING VOLUME THROUGH BRAIDING
The barrier to volume production has long constrained wider adoption of composites, particularly in automotive,
infrastructure and transport. Traditional composite processes often rely on labour-intensive layup or slow curing cycles, demanding either “a small army of people or some very, very expensive kit,” as Donegani puts it. Composite Braiding’s core process addresses this bottleneck directly. Using industrial braiding machines, the company produces continuous tubular preforms, or flexible composite “socks”, at exceptional speed. “One small braiding machine can produce about a mile of this a day,” Donegani says. “And that machine can be run by one person.” The implication for scalability is significant: fibre architecture can be created continuously, repeatably and with minimal labour input. These braided preforms are subsequently consolidated into fully
structural components using heat and pressure. The company specialises in hollow structural parts, from small, high-performance components for drones and bicycles through to largescale railway and bridge structures. However, producing the preform is only half the challenge; the second is moulding it fast enough to support volume manufacture. Historically, moulding highperformance composite parts has involved long cycle times. Composite Braiding has developed proprietary processes that compress moulding cycles from hours down to minutes. “We can mould something that would historically have taken several hours in just a couple of minutes,” Donegani notes, making high-throughput production viable.
www.engineerlive.com
27
COMPOSITES
ENERGY EFFICIENT PROCESSING
Volume alone is not enough if it comes at an environmental cost. Composites have traditionally delivered sustainability benefits through lightweighting, but concerns remain around embedded carbon and end-of-life disposal. Composite Braiding’s approach centres on blended thermoplastic composites, where reinforcement fibres and thermoplastic matrix fibres are integrated from the outset. Examples include carbon fibre with PPS, glass fibre with polypropylene, and glass fibre with nylon 6. These materials offer relatively low embodied CO2 and, critically, eliminate many energy- and waste-intensive steps associated with thermoset composites. “There’s no laminating, no resin infusion, no vacuum bagging, no water phase,” Donegani explains. “To make this into a structural part, we just need heat and pressure.” Equally important is how that heat is applied. Conventional oven-based moulding heats large air volumes and massive tooling structures to reach process temperature, which is an inherently inefficient approach. Composite Braiding has instead developed tooling that localises heat to the mould surface only. “The mould face is at about 280°C, and the rest of the structure never gets above room temperature,” says Donegani. The result is a claimed 97–98% reduction in processing energy compared with oven-based systems.
DESIGNING FOR COMPLEXITY AND PERFORMANCE
Alongside process development, the company has invested heavily in materials and design capability to support complex geometries. One example is an automotive A-pillar reinforcement originally designed in aluminium. The OEM found the geometry technically and economically unviable in metal and turned to Composite Braiding. The final solution - a single-piece braided and moulded composite - was produced from a simple cylindrical braid, with all geometric complexity introduced during moulding. “That was made in a single piece,” Donegani
28
www.engineerlive.com
The company has invested heavily in materials and design capability to support complex geometries
says, “just by braiding a big cylinder and using a novel mould.” The process also enables internal reinforcement features to be moulded integrally within hollow sections, opening up new opportunities for load path optimisation. Fibre orientation can be tuned continuously: 0° fibres for axial stiffness, ±45° for torsion, or near-90° for crush resistance. “That gives us a vast degree of tunability,” Donegani notes, allowing engineers to tailor performance while minimising material usage.
CIRCULARITY BY DESIGN
Thermoplastic composites also fundamentally change the end-of-life equation. Unlike thermosets, they can be remelted, reshaped or reprocessed. “If it’s just cosmetic damage, I can put it back in the mould tool it came out of and make it back into the same part,” Donegani explains. Fibres can also be recovered by melting out the matrix. However, true circularity extends beyond materials to assemblies. Composite Braiding has demonstrated fully mono-material structures such as beams, closure panels and even fasteners made from the same carbon fibre/PA6 composite. This eliminates dissimilar materials, adhesives and galvanic corrosion risks, while simplifying recycling. “At end of life, you haven’t got a bunch of different materials to deal with,” says Donegani. The company has even developed composite rivets with high pullout strength that can be installed and removed in seconds, enabling straightforward disassembly. “We’ve designed for disassembly as well,” he adds. Braiding also addresses another
long-standing issue in composites: production waste. Traditional prepregbased processes can generate 30–40% scrap. Continuous braiding reduces this to around 1%, limited mainly to startand end-of-run material—and that waste is reusable. Composite Braiding routinely compression-moulds offcuts into secondary products such as grab poles or panels, closing the loop further. “We put our 30–40% waste figure down to about 1%,” Donegani says. “And that 1% is all reusable as well.”
FROM AUTOMOTIVE TO RAIL
The culmination of these capabilities is visible in large-scale infrastructure projects, such as a cantilevered twintrack railway structure developed under a Connected Places Catapult programme. Measuring around eight metres tall with a 4.7-metre cantilever, the composite structure delivered a 44% weight reduction compared with steel. Reduced mass lowers transport, lifting, access road construction and possession-time costs, amplifying the value of lightweighting far beyond the component itself. The project has been described by a Tier 1 rail contractor as a “game changer.”
A SCALABLE PATH FORWARD
Taken together, high-speed braiding, energy-efficient thermoplastic processing and circular design principles point toward a more scalable and sustainable future for composites. As Donegani concludes, the challenge is no longer whether composites can deliver performance, but whether they can do so “at high volume, sustainably, and in the shapes that engineers actually need.”
Composites
Trade Association
Composites UK is the Trade Association for the UK composites industry. Across the UK each member of Composites UK receives the opportunity to: • • • • •
Save money Save time Boost their impact Expand their network Secure their future
Capitalise on the growth of the Global composites market and join the expanding list of Composites UK member companies today.
WHAT OUR MEMBERS SAY... “Composites UK has been really important to us as a company over the last few years. It provides access to industry specific advice that an SME like us would struggle to source otherwise. Additionally, the networking opportunities give us a place to keep upto-date with industry developments.” Lyndon Sanders, Director, Far-UK
“Our visibility across the composites community has not only increased since becoming members but also continues to allow us to deepen our knowledge about this innovative sector by working with our industry peers and specialists. Everyone at Composites UK is a pleasure to work with and we are looking forward to what is next in store.” Julia Loeser, Sales and Marketing, DK Holdings
CONTACT US claire@compositesuk.co.uk www.compositesuk.co.uk
COMPOSITES
AUTOMATING COMPOSITE MANUFACTURING Airborne and Lockheed Martin advance digital automation for composite manufacturing
A
irborne has entered a strategic collaboration with Lockheed Martin to develop next-generation automation systems for composite manufacturing, addressing growing demands for agility, throughput and digital integration in aerospace production. Announced in November, the project - Enhancing the digital thread for composites manufacturing - focuses on automated laminating and kitting systems capable of handling increasingly complex material types and geometries. The collaboration is being delivered under a Lockheed Martin Industrial Participation Programme and strengthens long-standing cooperation between Lockheed Martin and Dutch industry. From a manufacturing engineering perspective, the initiative targets one of the most challenging areas of composite fabrication: the efficient, repeatable preparation and placement of diverse ply materials while maintaining full digital traceability.
DELVING INTO THE TECH
At the technical core of the project is the evolution of Airborne’s existing Kit by Light (KBL) and Automated Ply Placement (APP) technologies. KBL systems guide operators through complex kitting processes using digitally driven visual cues, reducing errors and improving consistency when assembling multi-ply kits. APP extends automation into the placement phase, enabling precise deposition of composite plies with controlled orientation, overlap and material handling. By integrating these platforms more tightly, the partners aim to create an automated laminating and kitting system capable of packaging non-standard material shapes and mixed material systems with minimal manual intervention. A central objective is to strengthen the digital thread across composites manufacturing. This involves improved software integration between design data, material preparation, layup and inspection. For aerospace OEMs, such
30
www.engineerlive.com
Airborne’s Kit by Light system
integration is critical to maintaining configuration control, ensuring compliance and supporting scalable production rates. The enhanced systems are expected to support higher output rates, broader material compatibility, including advanced prepregs and dry fibre formats, and more sophisticated in-process inspection capabilities.
KNOWLEDGE-SHARING IS KEY
Lockheed Martin’s role in the project includes sharing technical knowledge and production requirements from its aerospace and defence programmes, ensuring that the resulting systems align with real-world manufacturing constraints. The developments will be tailored to support the specific needs of Lockheed Martin business units, but the underlying technologies are intended to be adaptable across a range of composite-intensive platforms.
APPLIED EXPERIENCE
Airborne brings more than three decades of experience in composites, having evolved from a composite parts manufacturer into a specialist developer of automated production systems for aerospace, defence, automotive and renewable energy sectors. This background enables the company to approach automation challenges with a deep understanding of both material behaviour and production engineering. James McLachlan, head of sales at Airborne, described the collaboration as a validation of the company’s technical direction, stating that it, “will
enable us to accelerate our mission of pushing the boundaries of automated composites manufacturing.” From Lockheed Martin’s perspective, the project represents an opportunity to integrate smart material kit creation with data-driven automation to support flexible, next-generation production systems. As Tara Thomasson, Lockheed Martin technical fellow, noted, the collaboration will “integrate smart material kit creation with advanced data-driven automation for a flexible production system.”
STRONGER TOGETHER
Beyond the technical outcomes, the project highlights the role of international industrial partnerships in advancing manufacturing innovation. Joe Krapf, Lockheed Martin industrial participation country manager, emphasised the mutual benefits, with Airborne gaining enhanced capabilities and Lockheed Martin securing access to advanced kitting and laminating systems for future production lines. Jan Cristiaan Dicke, commissioner for military production of the Netherlands, underscored the strategic importance of such collaborations in strengthening the Dutch Defence Technology Industrial Base through innovation in production processes as well as products. For professional engineers, the Airborne–Lockheed Martin collaboration signals a continued shift toward digitally integrated, highly automated composite manufacturing systems capable of meeting the aerospace industry’s increasing complexity, rate and quality demands.
COMPOSITES
E
NC North Composites Engineering Ltd Training Unique ‘know how’ based courses in Composite Design, Analysis and Manufacture Specialist in Aerospace, Marine, and Automotive sectors
Cleanroom Solutions Design, specification, set up and expansion of composite workshop and cleanroom equipment Design and manufacture of composite curing and repair equipment Ready to expand your horizons Email: info@northcompositesengineering.co.uk www.northcompositesengineering.co.uk
Pentagon delivers a full turnkey solution for plastic injection moulding from one site of UK Manufacture. DESIGN DEVELOPMENT MOULDING TOOLING BEYOND THE MOULD www.pentagonplastics.co.uk websales@pentagonplastics.co.uk Tel: +44 (0) 1403 264 397
www.engineerlive.com14/02/2025 31 14:12
1533425274-Print Ad Designs- 148x105mm-A6-V1-CS.indd 2
COMPOSITES
BIOCOMPOSITE
BOOM How biocomposites are gaining industrial momentum through functional and process innovation
B
iocomposites are moving rapidly from experimental materials into viable candidates for industrial applications, driven by advances in additive manufacturing, polymer chemistry, and sustainable process engineering. Recent research and collaborative development programmes demonstrate that bio-based and bioinspired materials are no longer limited to low-performance or disposable uses. Instead, they are increasingly being engineered to meet durability, manufacturability, and lifecycle requirements expected by professional engineers in sectors ranging from biopharmaceutical manufacturing to robotics and electronics.
SELF-HEALING POLYMERS
One key area of innovation is the development of self-healing polymer systems that draw inspiration from biological repair mechanisms. At the Rochester Institute of Technology (RIT), researchers led by Christopher Lewis are addressing one of additive manufacturing’s persistent challenges: brittleness and crack propagation in polymer-based components. Their work focuses on stimuliresponsive photopolymers capable of autonomously repairing damage, extending part service life and improving reliability in load-bearing applications. The materials under development are ultraviolet-curable resins used in lithography-based 3D printing processes. During printing, the liquid resin selectively solidifies layer by layer, forming a thermoset matrix combined with a thermoplastic
32
www.engineerlive.com
CAD rendering of a 3D printed media contact device used to continuously monitor media within a bioreactor via spectroscopy
additive. The self-healing behaviour arises from polymerisation-induced phase separation (PIPS), in which thermoset and thermoplastic phases separate dynamically during curing. This evolving microstructure allows thermoplastic domains to redistribute under stress or heat, reinforcing damaged regions and closing microcracks. In addition to self-repair, the material exhibits shape-memory behaviour, enabling components to recover their original geometry after deformation. Supported by the U.S. Department of Defense and conducted in partnership with RIT’s AMPrint Center, the project is now focused on optimising resin viscosity and light sensitivity to ensure consistent print quality. For industrial engineers, such multifunctional materials could reduce inspection intervals, lower maintenance costs, and expand the use of additively manufactured parts in demanding environments.
MORE SUSTAINABLE BIOCOMPOSITES
Beyond functional performance, sustainability is becoming a primary driver of materials innovation, particularly in sectors reliant on disposable polymer systems. In
the UK, Innovate UK’s £1.9 million Project Nexus exemplifies this shift. The collaboration brings together Photocentric, Sartorius, Metamorphic, CPI, and academic partners to develop bio-based materials for singleuse technologies (SUTs), such as bioreactors used in biopharmaceutical manufacturing. Single-use systems offer operational advantages including rapid deployment, reduced cleaning requirements, and lower consumption of water and chemicals. However, they also generate significant plastic waste. Project Nexus aims to reconcile these competing factors by developing bio-based, additively manufactured thermosets that can withstand autoclaving and be reused or more easily recycled at end of life. Central to the initiative is Photocentric’s JENI platform, an automated digital mass manufacturing system designed for high-throughput polymer production. By combining this platform with newly formulated bio-based resins, the consortium aims to deliver bioreactor components that maintain the flexibility of disposable systems while improving circularity. The resulting components will be evaluated for pharmaceutical R&D, point-of-care manufacturing,
COMPOSITES
and industrial biotechnology, including green chemical production. Importantly, the project also includes full technical, economic, and environmental assessments to support industrial adoption rather than isolated demonstration.
BIO-BASED FEEDSTOCKS
In parallel, researchers are exploring radically different bio-based feedstocks and manufacturing routes. At the University of Washington, a team led by Danli Luo has developed a mycelium-based biocomposite printing approach that eliminates the need for conventional moulds. Using a custom 3D printing system known as Fungibot and a printable paste called Mycofluid, structures are printed and then incubated to allow fungal mycelium to grow within the geometry. The resulting composite combines biological growth with digital fabrication, producing lightweight structures with low embodied energy. While mycelium composites are currently best suited to non-critical structural applications, their mouldfree processing and low material input are attractive for industrial designers seeking sustainable alternatives for housings, panels, or temporary structures. The approach also highlights how biological growth
Christopher Lewis, a faculty-researcher in RIT’s College of Engineering Technology, developed a self-healing materials solution to improve 3D printing. Image via Peter Schuck/RIT
processes can be integrated into manufacturing workflows rather than treated as post-processing steps. Other research groups are focusing on bio-based photopolymers compatible with high-resolution additive manufacturing. At Vilnius University and Kaunas University of Technology, scientists have developed a recyclable bio-resin derived from soybean extracts for Optical 3D Printing (O3P). The resin reportedly meets the mechanical and processing requirements of conventional photopolymers while
Photocentric’s fully automated digital mass manufacturing platform will be utilised in Project Nexus alongside the use of newly developed bio-based, eco-friendly materials
offering improved biocompatibility and reduced reliance on petroleumderived feedstocks. From an engineering standpoint, such materials are significant because they address two critical barriers to adoption: compatibility with existing equipment and predictable performance. By enabling small-batch and customised production without sacrificing material consistency, bio-resins of this type could find applications in medical devices, electronics enclosures, and specialist tooling. Taken together, these developments suggest that biocomposites are entering a new phase of industrial relevance. Rather than being defined solely by their environmental credentials, they are increasingly differentiated by functional performance, process integration, and lifecycle efficiency. Self-healing polymers improve durability, bio-based resins enhance circularity in singleuse systems, and biologically derived composites challenge conventional assumptions about how industrial materials are produced. For professional engineers, the challenge now lies in qualification, standardisation, and system-level integration. As these materials mature, biocomposites are likely to become not just sustainable alternatives, but enabling technologies for new product architectures and manufacturing strategies in a resource-constrained industrial landscape.
www.engineerlive.com
33
FASTENERS & SEALING
Peter Grant shares the findings from SPIROL’s recent whitepaper on the advantages of oval compression limiters
TALKING TOLERANCES
I
n multi-fastener plastic assemblies, maintaining precise alignment between components is often more complex than it initially appears. Even when each individual component meets its design tolerance, the combined effect - known as tolerance stackup - can create misalignment large enough to compromise fastener fit, structural integrity, or longterm joint performance. SPIROL’s recent white paper, ‘Absorbing Centreline and Stack-Up Tolerances with Oval Compression Limiters’, provides a detailed examination of how oval compression limiters can be strategically applied to absorb accumulated variation while ensuring consistent, repeatable alignment across multi-point assemblies.
UNDERSTANDING CENTRELINE TOLERANCE
Compression limiters are used in plastic components to prevent overcompression during fastening and to create stable load paths at bolted joints. When two or more fastening points exist within an assembly, the positional accuracy of each limiter relative to the others – its centreline tolerance - becomes critical. As the white paper notes, “centreline tolerance defines the maximum allowable misalignment between two or more components in an assembly.” If the limiters drift beyond this allowable window, fasteners may no longer align properly with the mating
34
www.engineerlive.com
SPIROL’s oval compression limiters Figure 1: Round Compression Limiters provide precise alignment but do not accommodate stack-up tolerances
component, forcing rework, assembly scrap, or design changes. Maintaining tight centreline tolerances is especially difficult in plastic parts, where moulding variation, shrinkage, and warpage can shift hole locations. When these variations accumulate across multiple features, the result is a classic tolerance stack-up scenario.
TOLERANCE STACK-UP
Tolerance stack-up refers to the accumulation of individual dimensional variations from each component in a system. Even when each part is manufactured within specification, their combined variation can exceed allowable positional limits. Figure 2: SPIROL’s Oval Compression Limiters compensate for misalignment by providing an extra 2.25mm of clearance on one axis
FASTENERS & SEALING
SPIROL’s paper raises a key design question: Will all fastening points still align at both the minimum and maximum stack-up conditions? In many assemblies, the answer is no – particularly when using rigid, round compression limiters that offer little accommodation for lateral deviation. The case study presented in the white paper (Figures 1 & 2) highlights this issue clearly.
MANAGING Y-AXIS DEVIATION
A design engineer managing a multipoint assembly needed to ensure that no movement occurred along the y-axis. To do this, they used one round compression limiter as a datum, installed first to lock the assembly’s reference position. However, the remaining three fastening points experienced positional variation that exceeded allowable centreline limits. Round limiters, while excellent for precise alignment, are unforgiving when misalignment occurs. As the white paper explains, “round compression limiters provide precise alignment but do not accommodate stack-up tolerances.” By replacing the remaining three round limiters with SPIROL oval compression limiters, the designer enabled controlled positional compliance where needed while maintaining an accurate datum at the primary fastening point.
THE ENGINEERING BEHAND OVAL COMPRESSION LIMITERS
SPIROL’s CL400 and CL460 oval compression limiters incorporate an elongated geometry that provides 2.25mm of additional clearance along one axis. This built-in compliance enables the assembly to absorb centreline variation without forcing the mating components out of alignment. Oval limiters are manufactured using a rolled-seam forming process that produces minimal scrap and supports high-volume manufacturing. According to the white paper, this results in “significantly lower costs compared to machined, cold headed, or powdered metal parts that can have costly unused material or slower production output.” In addition to better tolerance absorption, oval limiters maintain the
Figure 3: Misalignment of the final fastening point (bottom right) may cause issues during assembly
Figure 4: An Oval Compression Limiter placed diagonally in one corner accounts for misalignment
structural support required to protect plastic components during bolt tightening - ensuring joint integrity is not compromised.
ensures a secure assembly without forcing components into alignment or introducing residual stresses.
STRATEGIC USE IN COMBINATION
One of the paper’s most important insights is that oval compression limiters should not replace round limiters universally. Rather, the strongest designs use both strategically. Round limiters help maintain overall alignment by restricting excessive float along both axes. Oval limiters provide targeted compensation where misalignment is expected or unavoidable. SPIROL highlights that if too many oval limiters are used, “the entire plastic component could sit too far to one side of the mating component.” The engineered balance between the two shapes ensures structural stability while providing compliance only where needed.
MANAGING X-Y MISALIGNMENT IN A FOUR-POINT MOUNT
A second case study illustrates this strategy (Figures 3 & 4). In a fourpoint rectangular mounting pattern, misalignment can occur along both the x and y axes. The designer placed one oval limiter diagonally opposite the datum to absorb accumulated variation at the final fastening point. During assembly, three round compression limiters are fastened first, fixing the component’s global position. Then, any mismatch between the components is absorbed at the fourth location by the oval limiter. This
ENSURING SUCCESSFUL DESIGN INTEGRATION
The white paper concludes by emphasising that the wide variety of compression limiter geometries makes specialist support essential. SPIROL recommends consulting its Application Engineering team early in the design process to confirm the best limiter configuration for a specific assembly. With nearly 80 years of fastening and joining experience, SPIROL provides design guidance, tolerance analysis, and recommendations tailored to the specific materials, assembly loads, and manufacturing constraints of each application. Oval compression limiters offer engineers an effective solution for managing centreline tolerances and stack-up variation in multi-point plastic assemblies. By combining selective compliance with structural robustness, they enable more forgiving assembly processes, reduce the risk of misalignment, and improve overall product manufacturability. When used strategically with round limiters, oval limiters provide a cost-effective, highperformance method for absorbing accumulated tolerances without sacrificing the precision required in today’s engineered products.
Peter Grant is a sales application specialist at SPIROL Canada. www.spirol.co.uk
www.engineerlive.com
35
FASTENERS & SEALING
®
DS-DEC18-GEORGE EMMOTT CLOCK:DS-DEC18-GEORGE EMMOTT PRESSINGS 05/12/2018 11:46 Page 1
36
www.engineerlive.com
FASTENERS AND SEALING
AEROPASTE
ADHESIVES Enabling next-generation aerospace bonding with paste adhesives
A
dhesive bonding has become a critical enabling technology in modern aerospace manufacturing, supporting the industry’s push toward lightweighting, sustainability, automation, and high-rate production. Against this backdrop, Syensqo is advancing the role of paste adhesives as flexible, high-performance alternatives to traditional joining
methods. According to Juan Abad Zapatero, customer engineer at Syensqo, these materials are designed not only to meet demanding structural requirements, but also to integrate seamlessly into evolving aerospace manufacturing ecosystems. Syensqo was established in December 2023 following the separation of Solvay into two independent companies. While Solvay
retained its essential chemicals business, Syensqo emerged as a science-driven materials specialist focused on high-performance polymers, composites, and specialty solutions. The company’s name deliberately references Solvay’s scientific heritage, including the historic Solvay Conferences of the early 20th century that brought together figures such as Albert Einstein and Marie Curie. Today, Syensqo employs around 13,000 people across 30 countries, with more than 16 industrial sites and major R&D centres supporting markets such as aerospace, mobility, energy, and electronics.
ADHESIVES IN THE AIR
Juan Abad Zapatero, customer engineer at Syensqo, speaking at Advanced Engineering
From an aerospace perspective, Syensqo’s portfolio spans carbon fibres, prepregs, resins, primers, surface films, film adhesives, and paste adhesives. These materials are used across fixed-wing aircraft, rotorcraft, advanced air mobility platforms, propulsion systems, and space and launch applications. Adhesives, in particular, are increasingly central as aircraft structures evolve toward multi-material designs and higher levels of automation. “Unlike mechanical fasteners or welds, adhesives distribute loads evenly across the joint area, avoiding local stress concentrations,” explains Zapatero. This improves fatigue resistance and long-term durability, while also enabling secondary functions such as sealing against
www.engineerlive.com
37
FASTENERS AND SEALING
moisture, air, and chemical ingress – critical for corrosion protection in metallic structures. Adhesives also dampen vibration and noise, a benefit that is especially relevant for emerging electric and advanced air mobility platforms. Weight reduction is another key driver. Mechanical fasteners add mass and require overlapping structures, whereas adhesive bonding can reduce both thickness and part count. In addition, adhesives enable greater design freedom, allowing engineers to join dissimilar materials, bond thin or complex geometries, and achieve smooth, aerodynamically clean surfaces. From a manufacturing standpoint, adhesives are also well suited to high-rate and automated production, aligning with the aerospace industry’s push for cost efficiency.
FILM VS PASTE ADHESIVES
Within Syensqo’s adhesive offerings, two product forms dominate aerospace applications: film adhesives and paste adhesives. Film adhesives are well established in primary structures, offering excellent toughness, environmental resistance, and controlled bondline thickness. Paste adhesives, however, are gaining increasing attention due to their process flexibility and compatibility with automation. Paste adhesives are designed to deliver film-adhesive-like performance in a paste format. “Paste adhesives combine high strength, high toughness, and excellent hot–wet performance for both bonding and repair of metallic and composite substrates,” Zapatero says. They can be cured in an autoclave, out of autoclave, or even at ambient conditions, with a wide range of cure temperatures and cycle times. This flexibility is particularly valuable for large structures, repairs, and ratedriven production environments. Paste systems are available as onecomponent premixed formulations or two-component systems that are mixed at the point of use. The latter offer improved storage stability and do not require freezer storage. Despite their relatively high viscosity, these adhesives are thixotropic and slumpresistant, allowing application on non-
38
www.engineerlive.com
Syensqo Headquarters
horizontal surfaces while still flowing under shear during dispensing. Crucially, Paste adhesives are well suited to automated application. They can be dispensed using pumping and metering equipment, placing precisely the required amount of material exactly where it is needed. “That capability has a very powerful impact in terms of cost efficiency,” Zapatero notes, citing reduced material waste, lower capital expenditure, elimination of autoclaves in some cases, and faster cycle times.
THE AEROPASTE PORTFOLIO
Building on this foundation, Syensqo has introduced Aeropaste, a new generation of epoxy-based structural paste adhesives tailored for aerospace applications. The Aeropaste portfolio is designed to address challenges including lightweighting, cost reduction, processing flexibility, and high-rate manufacturing. Available in both oneand two-component variants, Aeropaste products cover a broad range of cure temperatures and schedules. Aeropaste systems are optimised for bonding and repair of metallic structures while maintaining filmadhesive-like mechanical performance. They offer a strong balance of shear and peel strength, are highly toughened, and retain performance in hot and wet service environments. Another key advantage is tolerance to bondline thickness variation, which simplifies manufacturing and supports automated deposition. Gap-filling capability further enhances design freedom for components with nonuniform bondlines. Ease of use is also a defining feature. One-component systems can be dispensed directly from cartridges using standard electric guns, while twocomponent systems rely on integrated
static mixers with fixed mix ratios, avoiding complex calculations. Shelf life typically ranges from six to twelve months, and open times can vary from minutes to several hours depending on formulation and conditions. Beyond the adhesive itself, Zapatero emphasises that durable bonding depends fundamentally on surface quality: “Adhesion depends on something you can’t see – the chemical condition of the surface.” To address this, Syensqo has partnered with Brighton Science to apply surface intelligence tools based on precise measurement of surface energy via water contact angle analysis. Unlike traditional methods such as waterbreak tests, this approach provides quantitative, non-destructive, and repeatable data. Using portable and automationcompatible equipment, manufacturers can assess surface cleanliness, activation, and aging in real time, directly on the production floor. This enables validation of surface readiness prior to bonding and tighter control over variability introduced by surface preparation methods such as abrasion, plasma, or flame treatment. Importantly, surface energy is not static; it degrades with time, humidity, temperature, and handling. By monitoring these effects, Syensqo aims to help customers define optimal processing windows and storage protocols. The company’s Aeropaste adhesives, combined with data-driven surface intelligence, illustrate how adhesive bonding is evolving from a materials choice into an integrated engineering system. For aerospace engineers facing increasing pressure to deliver lighter, more sustainable, and more affordable aircraft, these innovations position paste adhesives as a cornerstone of next-generation structural design and manufacturing.
FASTENERS & SEALING
» WEH® QUICK CONNECTORS Pressure-tight connections in SECONDS » Just PUSH to connect -
No hand tightening, no tapes, no thread sealants » Direct connection to threads, beads, tubes etc. » Pressure range of up to 14,500 psi
WEH UK enquiries@wehuk.co.uk T: 01527 573010
» www.weh.uk
Threaded Threaded insert insert solutions solutions from an expert team from an expert team We are globally-renowned specialists with a 60-year legacy We aremanufacture globally-renowned specialists a 60-year legacy in the of threaded insertswith for plastics, light in the manufacture of threaded inserts for plastics, light metal alloys and composite materials. metal alloys and composite materials. We hold millions of items in stock for quick delivery and We millionsdesign of items in stock for quick delivery and offerhold a bespoke service. offer a bespoke design service. Whether you’re designing a new component or troubleWhether you’re designing a new component orare troubleshooting an existing one, our technical experts here shooting an existing our team, technical are here to help. With Tappex one, on your yourexperts small parts won’t to help. With Tappex on– your team, your small parts won’t become big problems they’ll be the building blocks of your become big problems – they’ll be the building blocks of your next great design. next great design.
UK & Europe: sales@tappex.co.uk UK & Europe: sales@tappex.co.uk North America: sales@tappexinserts.com North America: sales@tappexinserts.com
www.engineerlive.com
39
MOTORS, DRIVES & CONTROLS
Configurator LR 5 operated via Procan Alpha 6
INTEGRAL INTEGRATION Dr Boy’s head of electrical engineering, Thomas Kühr, explains how to achieve increased efficiency through integral robot integration
I
n the highly competitive manufacturing industry, especially in injection moulding, automation with robot systems is a critical factor for optimising process parameters, increasing production output and ensuring consistent product quality. Maximising this potential requires a system integration of robotics into the central machine control system. Dr Boy’s Procan Alpha 6 control system defines a new standard by implementing a profound and comprehensive robot integration that goes beyond conventional interface functionalities.
40
www.engineerlive.com
A HOLISTIC CONTROL ARCHITECTURE
represents a fundamental aspect of integration. All process-relevant parameters – from the mould opening position and cycle time up to specific ejector kinematics – are exchanged in real time between the injection moulding machine and the LR 5. This eliminates duplicate data entry, minimises the risk of configuration errors, and significantly reduces setup times.
BIDRECTIONAL DATA COUPLING
CONSOLIDATED ALARM SYSTEM AND EVENT-LOGGING
The complete integration of LR 5 into the Procan Alpha 6 control system transforms the manufacturing cell of individual components into an intelligent system. This architectural consolidation means significant advantages in terms of humanmachine interface (HMI), data management and process reliability.
The automatic, bidirectional data coupling of the LR 5 with the data set of the injection moulding machine
A consolidated alarm system and event-logging are crucial for proactive
MOTORS, DRIVES & CONTROLS
fault diagnosis and the maximisation of the plant availability. All malfunctions, warnings, and operating events generated by the injection moulding machine or the LR 5 are compiled in a central logging system. This provides operators with a comprehensive and consolidated overview of the system status of the entire production cell. The efficiency of the cause analysis is increased and unplanned downtimes are minimised. The restart after a malfunction is significantly simplified, as all position data is known, which prevents collisions.
Dr Boy’s Procan Alpha 6 control system defines a new standard by implementing a profound and comprehensive robot integration that goes beyond conventional interface functionalities
HOMOGENEOUS HMI
The homogeneous HMI structure, which corresponds to that of the injection moulding machine, is crucial for user acceptance and operational efficiency. Operators familiar with the Procan Alpha 6 can operate the robot functions without extensive additional training. The uniform user interface, consistent menu navigation, and familiar graphical visualisation drastically reduce the training period and enable fast and reliable programming.
SHARED USE
The option to share freely programmable I/O interfaces simplifies the integration of peripheral devices and the implementation of complex automation tasks. Sensors, external actuators, or other additional modules can be controlled and monitored via the shared I/O infrastructure of both systems - the injection moulding machine and the LR 5. This significantly reduces costs.
EXTENDED RANGE OF FUNCTIONS
In addition to the deep system integration, the robot functionality in the Procan Alpha 6 control system offers a comprehensive portfolio of application-specific functions. A freely configurable reference run including pneumatic axes is essential for precise initialisation of the robot after a system restart or a mould change. The inclusion of pneumatic axes, which are often used for fast gripping or depositing movements, ensures the exact calibration of the entire robot system. This increases the process reliability and the repeatability accuracy of the processes.
Boy 80 Electric with integrated LR 5
The ability to create freely configurable operation sequences with synchronised ejector kinematics allows the robot movements to be optimally coordinated with the injection moulding process. The robot can adapt its removal movement perfectly to the ejector stroke and the ejector speed. That means a gentle component removal, the avoidance of damage, and the minimisation of cycle time. Meanwhile, the electronic gearbox for ejector synchronisation is a function that kinematically couples the robot movement with the ejector movement of the injection moulding machine. This synchronisation ensures an optimum part transfer, with the component being gently and precisely taken over by the ejector. Similar to
ejector synchronisation, the electronic gearbox for mould movement synchronisation enables precise coupling of the robot movement with the mould opening and closing movement. This function is perfect for applications in which the robot must precisely place inserts into the mould or remove complex sprue systems during the mould opening process. Additionally, the integrated palletising functionality automates the end-of-line process. Users can define various palletising patterns to efficiently stack components on pallets, in containers, or other means of transport. This increases the degree of automation of the production line, reduces manual labour, and optimises post-injection moulding processes.
www.engineerlive.com
41
MOTORS, DRIVES & CONTROLS
Mark Rutherford, CEO of Alexander Battery Technologies
Regulation is becoming an increasingly important influence on design
Developing a battery system for a robotic platform extends well beyond selecting cells and designing a housing
Alexander Battery Technologies’ production facility
RELIABLE ROBOTS Mark Rutherford, CEO of Alexander Battery Technologies, on designing battery systems that support reliable robotic performance
B
attery behaviour plays a central role in determining how a robot performs throughout its working life. Yet, it is still common for assumptions to be made early on, before engineers have enough information to guide accurate design decisions. Robots rarely operate under uniform conditions, and their power requirements shift with load, temperature, duty cycle and environmental exposure. When engineering teams understand these conditions from the outset, they can create battery systems that deliver predictable and consistent performance. When these details
42
www.engineerlive.com
remain vague, the pack could be the first part of the system to show stress once the robot enters service.
BUILD THE PICTURE EARLY
The most effective development programmes start by building a realistic picture of the robot’s operating life. Engineers assess how long each duty cycle lasts, how sharply current rises during acceleration or lifting, how temperatures fluctuate across a shift and how frequently the robot can return to charge. This early definition influences every downstream
decision, from cell selection and thermal design to electrical protection and enclosure layout. A robot that runs continuously in a controlled warehouse may experience steady temperatures and modest vibration, while a platform working in semi-outdoor or industrial settings must cope with heat, moisture, dust, rapid load variations and sustained vibration. These conditions affect how cells age, how thermal management must be configured and how the control electronics respond during peak demand. If this information is not captured early, the design may perform well in a laboratory setting
MOTORS, DRIVES & CONTROLS
but deteriorate more quickly when exposed to real operating conditions. Once the operating profile is established, development benefits from a structured sequence of stages. Teams make better progress when detailed requirements are agreed before design work intensifies, rather than refining the brief while drawings evolve. A defined designreview stage ensures that electrical architecture, mechanical layout, thermal management and protection electronics still match the agreed requirements, rather than being updated in isolation. A later costfreeze point confirms materials, tooling and supplier arrangements, reducing the risk that commercial adjustments force technical compromise. These stages maintain consistency between disciplines and help prevent late-stage rework.
CHEMISTRY SELECTION AND DEFINING LIFETIME PERFORMANCE
Chemistry choice determines how the battery behaves under load, at varying temperatures and over repeated cycles. Lithium-ironphosphate offers strong cycle life and stable thermal behaviour, making it suitable for robots that must operate reliably for long periods without complex cooling. Nickelmanganese-cobalt provides higher energy density, supporting compact designs or lighter platforms that must move quickly or operate in tighter spaces. Lithium-titanate enables rapid charging and remains effective at low temperatures, which benefits fleets requiring fast turnaround or those working in variable climates. No chemistry is universally superior; the most appropriate option emerges when duty cycle, mass limits, thermal environment and charging strategy are considered together rather than as separate choices. Equally important is defining how much usable capacity the robot must retain at the end of the battery’s service life. Many platforms depend on consistent runtimes to complete routes or maintain production schedules. If the battery only meets that requirement when new, operators will experience declining
Chemistry choice determines how the battery behaves under load, at varying temperatures and over repeated cycles
performance, inconsistent shift lengths or unplanned charging as the pack ages. Conversely, if engineers build in excessive spare capacity, the robot carries avoidable cost and weight. Designing for a realistic end-of-life capacity helps ensure predictable ageing and alignment between laboratory measurements and field behaviour. Clear communication between robotics teams and battery engineers reduces misunderstandings around expected performance, margins and degradation.
MANAGING DEVELOPMENT WORK AND REGULATIONS
Developing a battery system for a robotic platform extends well beyond selecting cells and designing a housing. Engineers carry out simulation work, thermal modelling, electrical protection design, firmware development, mechanical integration, prototype builds and several rounds of validation testing. These tasks form the non-recurring engineering effort that turns a concept into a production-ready system. When planned from the outset, they allow engineers to test manufacturability, safety and performance in parallel, reducing the risk that changes in one area undermine another. A structured approach to non-recurring engineering also improves schedule
accuracy and reduces the number of prototype iterations required. Regulation is becoming an increasingly important influence on design. The introduction of the digital battery passport for systems above 2kWh will require detailed traceability accessible through a QR code. This includes information such as cell origin, manufacturing records, firmware versions and other process data. Incorporating traceability into the design ensures that compliance does not depend on reconstructing information after production has begun. Structured data also strengthens field diagnostics, supports audits and simplifies responsible end-of-life management. Although the requirement originates in regulation, it offers long-term operational benefits when implemented correctly. Reliable robotic performance comes from defining the operating environment thoroughly, choosing chemistry based on evidence, following structured development stages and embedding traceability from the beginning. When these foundations are in place, the battery becomes a stable and predictable part of the system that supports consistent performance throughout the robot’s life. When they are missing, the battery often becomes the component that limits capability, causes downtime or increases long-term cost.
www.engineerlive.com
43
SKILLS ZONE
BUILDING BRITAIN’S BATTERY WORKFORCE Why skills will decide the future transition to electric vehicles
Jonty Deeley-Williamson, head of learning and development at UKBIC, speaking at Advanced Engineering
B
y any measure, the UK’s transition to electrified transport is accelerating. Gigafactory announcements, electric vehicle (EV) targets and investment in battery research dominate headlines. Yet, as Jonty Deeley-Williamson, head of learning and development at the UK Battery Industrialisation Centre (UKBIC), argues, there is a critical enabler that remains consistently underplayed: skills. Speaking to an audience of engineers and industry leaders at Advanced Engineering, DeeleyWilliamson was direct about the challenge. “People keep telling me how great their technology is, or how electrification will magically solve everything,” he said. “But when I ask about skills, I get blank looks. These factories don’t run themselves.”
UKBIC’S ROLE IN THE BATTERY ECOSYSTEM UKBIC occupies a unique position in the UK and global battery
44
www.engineerlive.com
landscape. Based in Coventry, it is the world’s only open-access battery manufacturing facility covering the full process chain from electrode manufacture through to module and pack assembly. Crucially, it does not retain intellectual property. Instead, it exists to de-risk manufacturing scaleup and develop capability. “We’re not here to own IP,” Deeley-Williamson explained. “What we care about is making sure people can actually run these processes at scale.” That focus is timely. Around 65,000 new jobs are expected to be required across the UK battery supply chain as electrification accelerates. Without a coordinated approach to skills development, there is a real risk that capital investment in factories and R&D will outpace the availability of a trained workforce.
A WIDENING SKILLS GAP
The UK currently has only two confirmed large-scale battery manufacturing projects under
construction: AESC in the North East and Agratas in the Midlands. To meet projected automotive demand alone, the UK would need to roughly double its planned gigafactory capacity. That figure excludes additional demand from heavy goods vehicles, offhighway machinery, rail, marine and stationary energy storage. “These numbers are still educated guesses,” Deeley-Williamson noted. “But even the conservative estimates show we are several gigafactories short – and every one of those needs hundreds, if not thousands, of skilled operators and technicians.” Compounding the issue is the reality that electrification is not a simple workforce transition from internal combustion engines (ICEs) to batteries. For the foreseeable future, both technologies will coexist. That limits the pool of experienced workers who can be directly redeployed. “We’re not just flipping a switch,” he said. “You can’t assume the existing ICE workforce will simply move across. Many of the roles are different,
SKILLS ZONE
and we need new entrants as well as reskilled staff.”
MANUFACTURING AT ALL LEVELS
According to Deely-Williamon, persistent misconception is that battery manufacturing is dominated by PhD-level scientists. In reality, around 80–90% of roles in a gigafactory are Level 2 or Level 3 technical and vocational positions. “This is normal manufacturing, just cleaner,” he said. “Production operators, maintenance technicians, quality technicians - these are the backbone of the industry.” Each gigawatt-hour of battery manufacturing capacity typically supports around 180 direct manufacturing jobs, with at least 120 linked to automotive supply. As capacity scales, job creation is broadly linear. This has significant implications for education policy. While the UK has strong universitybased battery research through organisations such as the Faraday Institution, vocational education and further education colleges have historically been under-supported. “We’ve invested heavily in universities, but we’ve left vocational education behind,” Deeley-Williamson said. “If we lose people at Level 2 and Level 3, the whole system falls over.”
TRANSFERABLE SKILLS: A HIDDEN ADVANTAGE Despite the scale of the challenge,
Projected employment supported by the EV and battery industry in 2040
Deeley-Williamson is optimistic. Many of the core skills required for battery manufacturing already exist in adjacent industries. “If you walk through a battery plant, you’ll be surprised how much of the equipment comes from elsewhere,” he said. “Mixers came from concrete and food processing. Cell assembly looks a lot like electronics manufacturing. Maintenance and machine minding are universal skills.” This creates an opportunity to reskill workers from industries in decline, rather than starting from scratch. Process control, statistical analysis, equipment maintenance and quality assurance are all transferable competencies.
Upcoming UKBIC opportunities for battery manufacturing training
UKBIC has built a structured skills ecosystem spanning Levels 2 to 5, complementing higher-level academic provision. Its training portfolio ranges from introductory courses explaining battery manufacturing fundamentals to deep-dive, hands-on experience on a live production line. “We’re currently the only place in the world where you can get lineside experience in a real battery manufacturing environment,” DeeleyWilliamson said. “Most commercial plants won’t let you anywhere near their lines.” UKBIC has also led the development of the UK’s first Battery Manufacturing Technician apprenticeship standard, now adopted internationally in countries including Germany, France and Singapore. Additional short courses are being developed to support automotive workers, service leavers and those transitioning from ICE manufacturing. Batteries account for around 62% of the value and weight of an electric vehicle. If the UK fails to build them domestically, it risks higher import costs, exposure to trade barriers and the loss of a strategically important manufacturing sector. “We’re already seeing what happens when we don’t act,” Deeley-Williamson warned, pointing to the dominance of Asian manufacturers, who currently account for around 94% of global battery production. “This isn’t about losing a niche industry – it’s about losing the heart of future vehicle manufacturing.”
www.engineerlive.com
45
SKILLS ZONE
Professional-grade site tools enable apprentices to complete their programmes, master technical skills, and build a stronger and more confident workforce without delaying projects further
Engineering apprenticeships have seen a decline in completion rates
THE APPRENTICESHIP GAP Data reveals an acute shortfall threatening the UK’s technical workforce
T
he UK engineering sector is entering one of its most acute workforce shortages in decades, with new data revealing a widening disconnect between labour market demand and the country’s apprenticeship
pipeline. According to DART Tool Group’s Apprenticeship Gap Report, engineering now faces the most severe deficit of all technical trades analysed, with 145 job openings for every one completed apprenticeship – equivalent to more than 46,000
unfilled engineering positions. For a sector responsible for national infrastructure, manufacturing productivity, energy security and industrial innovation, the risk is structural, not cyclical. Employers are encountering escalating recruitment
LARGEST DEFICITS BY ENGINEERING SPECIALISM
Trade Job Openings Completion Rate per Completer (2024/2025) Engineering Maintenance 546:1 34% Mechanical Engineering 488:1 56% Engineer (generalist) 367:1 100% (but almost no starters) Maintenance Technician 119:1 Low Engineering Technician 114:1 60% Fitter 73:1 27% Building Services Engineer 47:1 22%
46
www.engineerlive.com
SKILLS ZONE
decline at a time when mechanical skills underpin major sectors such as manufacturing automation, aerospace, renewables and transport. General engineering roles saw the sharpest decline in new starters: 83% drop year-on-year, 97% drop since 2021/22.
LOW COMPLETION RATES
Engineering apprenticeships have seen a sustained fall in completion outcomes: 45% in 2024/25 50% in 2023/24 42% in 2022/23 33% in 2021/22 While the long-term trend is improving compared to 2021/22, the recent drop from 50% to 45% is a reversal at precisely the wrong moment.
AN AGEING WORKFORCE
delays, rising project backlogs and an increasingly ageing workforce. This analysis examines the engineering skills deficit through a technical and workforce-planning lens, drawing out implications for engineering managers, project leaders and industry strategists.
A DATA-DRIVEN VIEW
Across all six trades analysed – engineering, construction, electrical, plumbing, manufacturing and building services – the study found only 809 apprenticeship openings available to fill over 86,000 job vacancies nationwide. This translates into a sector-wide ratio of 106 vacancies per apprenticeship, but engineering sits significantly above that average. Engineering maintenance is the most heavily constrained discipline, with nearly 550 vacancies for every newly qualified apprentice. Completion rates of just 34% compound the issue. Mechanical engineering follows closely at 488:1, with apprenticeship starts falling by 52.6% year-on-year and down 18.2% since 2021/22 – a worrying
Around 20% of UK engineers are due to retire within five years, according to the report. Many who remain in the sector are transitioning into supervisory or managerial roles, reducing the pool of technically hands-on mentors. Apprentices entering the workforce encounter fewer experienced engineers available to provide the practical, nuanced guidance needed for equipment operation, fault diagnostics, system commissioning and site safety.
OUTDATED PERCEPTIONS
Despite the increasing sophistication of engineering – including digital twins, robotics integration and smart manufacturing – apprenticeships still suffer from outdated stereotypes. Many young people and parents remain unaware of the technical, wellpaid and often future-facing nature of modern engineering roles.
TRAINING INFRASTRUCTURE MISALIGNMENT
The report highlights gaps in regional provision, limited on-site learning flexibility and an oversupply of learners in trades with limited local employment opportunities and vice versa. Engineering employers still report difficulty accessing
aligned training, particularly in more specialised roles such as mechatronics, controls engineering and building services engineering.
STRATEGIC RECOMMENDATIONS
Ryan Paterson, managing director at DART Tool Group, emphasises that “with a stronger, more effective apprenticeship system and active encouragement and promotion of trade industry jobs, the risk of a widening skills gap can be reduced.” Engineering employers can help shape curricula, modernise workshop equipment and ensure trainers remain up to date with evolving industrial technologies. Direct collaboration also increases visibility of apprenticeship pathways. Many small and mediumsized engineering firms struggle to release staff for extended off-site blocks of training. Hybrid models that combine digital learning, modular assessments and integrated jobsite experience would enable more apprentices to complete programmes. Data shows that engineering apprentices often leave programmes due to workload conflicts, lack of progression clarity or insufficient technical mentorship. Structured mentoring models, early-career skills bootcamps and access to high-quality tools and equipment can materially influence completion outcomes. Paterson notes, “professional-grade site tools enable apprentices to complete their programmes, master technical skills, and build a stronger and more confident workforce without delaying projects further.”
ADDRESSING THE CHALLENGE
The Apprenticeship Gap Report provides a detailed analytical snapshot of a talent pipeline under significant strain. With tens of thousands of engineering roles unfilled, retiring experts leaving technical gaps, and completion rates falling, the sector faces a multifaceted challenge. But the report also points toward solutions: smarter workforce planning, deeper industry–education collaboration, and investment in the tools, technologies and training methodologies that support successful apprenticeship outcomes.
www.engineerlive.com
47
SHOW PREVIEW
J
CONNECTING THE COMPOSITES COMMUNITY
EC World 2026 returns to Paris as the world’s leading international exhibition dedicated to composite materials and their applications, offering an unrivalled platform for innovation, collaboration and business development across the global composites value chain. Organised by JEC Group, the non-profit organisation entirely dedicated to promoting composite materials worldwide, the event continues a legacy that dates back more than 60 years. Taking place over three intensive days, JEC World 2026 will welcome more than 46,000 professionals, 1,400 exhibitors and participants from over 100 countries. Engineers, designers, researchers, buyers and decision-makers will come together to explore how composites are transforming industries ranging from aerospace, automotive and construction to renewable energy,
JEC World take place 10-12 March 2026
48
www.engineerlive.com
medical devices and sports equipment. At the heart of the event is JEC’s mission to accelerate the adoption of composites across all application sectors. The show highlights the unique properties of composite materials - lightweight strength, corrosion resistance, design flexibility and durability - and demonstrates how advances in materials, processes and automation are enabling higher performance with lower environmental impact. Exhibitors will showcase innovations including lowcarbon fibres and resins, automated manufacturing technologies such as RTM, infusion and 3D printing, recycling solutions and smart, sensorintegrated structures. JEC World is also renowned for its high-quality content and networking opportunities. A tailored business meetings programme facilitates targeted one-to-one meetings, enabling participants to build partnerships and
accelerate projects. The conference programme features case studies, technical sessions, market outlooks and panel discussions addressing key challenges such as circularity, carbon reduction and industrial scalability. In partnership with SAMPE, dedicated technical sessions provide deep insight into advanced materials and manufacturing methods for engineers and scientists. From Innovation Planets and live demonstrations to the Startup Booster competition and Innovation Awards, JEC World 2026 offers a comprehensive view of where composites are heading next. More than a trade show, it is the must-attend global meeting point for anyone shaping the future of composite materials.
For more information visit: www.jec-world.events
SHOW PREVIEW
S
INNOVATION IN INDUSTRIAL TECHNOLOGY
outhern Manufacturing & Electronics returns to Farnborough International Exhibition Centre from 3–5 February 2026, reaffirming its position as the UK’s largest annual industrial technology event. Free to attend and spanning three days, the show is a must-visit for professionals across engineering, manufacturing and electronics who want early access to the latest technologies, suppliers and ideas shaping the future of industry. Now in its 27th year, Southern has evolved from a regional, familyrun exhibition into a nationally and internationally recognised showcase, attracting around 10,000 attendees and more than 550 exhibitors. Located just 30 minutes from London, the event brings together
OEMs, SMEs and start-ups from across all sectors, offering extensive opportunities to network, exchange best practice and build long-term partnerships. The exhibition floor will feature thousands of products and solutions covering machinery, production equipment, electronic design and assembly, tooling, components and subcontract services. Visitors can see cutting-edge technologies up close, engage directly with suppliers and identify innovations that can strengthen their supply chains and improve operational performance. A key draw is the show’s freeto-attend, CPD-accredited seminar programme, delivered across two technical streams. The Engineering Seminar will address topics such as the path to operational excellence,
digital transformation, process optimisation and lessons learned from leading manufacturers. In parallel, the Electronics Seminar will explore how manufacturers are overcoming challenges through automation, Industry 4.0 and the practical adoption of advanced technologies, including additive manufacturing. Live demonstrations and expertled sessions will provide practical insights into integrating digital tools, improving productivity and unlocking new growth opportunities. Whether sourcing new materials, evaluating production technologies or seeking inspiration for digital transformation, Southern Manufacturing & Electronics 2026 offers a comprehensive, futurefocused experience.
SM&E takes place 3-5 February 2026
For more information visit: www.southern-manufacturing-electronics.com
Cirrus Research
19
Composites UK
29
Curtiss-Wright
25
EOS
10
Emmott Springs
36
JEC World 2026
26
LMI Technologies
10
North Composites Engineering
31
Pentagon Plastics
31
Plastic Coatings
31
Index to advertisers
Plastic Products International
Spirol
36
IBC
Star Fasteners
OBC
RM Fowler
19
Tappex Thread Inserts
39
TLX Technologies
5
WEH UK
39
Spectrum Instrumentation
IFC
www.engineerlive.com
49
GET INVOLVED e advertising@setform.com t +44 (0)207 253 2545
YOUR GUIDE TO DISTRIBUTORS, SUPPLIERS AND MANUFACTURERS IN THE INDUSTRY
Boker’s Inc.
Gold & Wassall Hinges
HIOKI
Boker’s, Inc., is a full-service manufacturer of precision metal stampings, washers, spacers and shims. Since 1919, nearly every industry around the world has trusted Boker’s to provide quality made-to-order components, world-class service and fast delivery.
With over two centuries of experience in the hinges industry, Gold and Wassall provides a fully comprehensive design and manufacturing service for any kind of hinge for practically any application.
HIOKI, founded in Japan in 1935, leads precision test and measurement technology. Renowned for advanced electrical current sensors, power electronics, and battery solutions, we deliver uncompromised accuracy and innovation built and engineered in Japan.
T +1 612 729 9365
T +44 (0)1827 63391
T +49-(0)6196-76515-0
E sales@bokers.com
E enquiries@goldwassallhinges.co.uk
E hioki@hioki.eu
W bokers.com
W goldwassallhinges.co.uk
W shop.hioki.eu/
LMI Technologies
Nano Dimension
North Composites Engineering
As the global leader in 3D scanning and inspection, LMI Technologies works to advance quality and productivity with 3D sensor technology.
Nano Dimension (Nasdaq: NNDM) aims to revolutionise electronics and mechanical manufacturing through precision additive manufacturing and AI-driven solutions, enabling on-demand production and managing a distributed manufacturing network.
A highly professional company who over the last 14 years have trained and actively empowered the composite sector. Experts in composite services, we provide world class training, consultancy and equipment to the Aerospace, Marine, Wind Turbine and Automotive sectors.
T +1 857-557-8022
T +44 (0) 1942 665292
E contact@lmi3d.com
E sales@nano-di.com
E info@northcompositesengineering.co.uk
W lmi3d.com
W nano-di.com
W www.northcompositesengineering.co.uk
PCE Instruments
RECOM Power
Rutland Plastics
Develops, manufactures and distributes test instruments, scales and balances and selected laboratory equipment for industry, trade and research. In addition to pre- and after-sales support, calibration and repair are also offered.
RECOM produces standard and custom DC/ DC, AC/DC converters, switching regulators, and LED drivers from sub-1W to tens of kW. Headquartered in Gmunden, Austria, RECOM is known for quality, innovation, wand excellent customer service.
With 70 years of experience, we offer a full range of plastic injection moulding services across all sectors with the ability to make plastic parts from 1g to 45kg and up to 1.5m in size.
T +44 (0) 161 464902 0
T +43 7612 883 25 700
T 01572 723476
E info@pce-instruments.co.uk
E info@recom-power.com
W www.pce-instruments.com
W recom-power.com
E enquiries@rutlandplastics.co.uk W www.rutlandplastics.co.uk
www.engineerlive.com
xx
The ONLY Partner YOU Need With over five decades of industry experience, Plastic Products International has established itself as a premier provider of high-quality manufacturing solutions. Since our founding in 1968, we have been dedicated to delivering “World Class Service,” a commitment that remains at the heart of everything we do. We specialise in a wide range of production services designed to take your project from concept to completion. Design & Toolmaking: Our team provides expert guidance in the initial stages of product development alongside our in-house Toolroom who can handle any tooling requirements. Injection Moulding: We provide precision moulding services backed by decades of technical expertise. Assembly & Finishing: We offer full assembly services and specialised Tampo Pad Printing for a professional final finish. 3D Printing: Utilising modern technology to support rapid prototyping and specialised production needs. Quality is the foundation of our operations and we maintain rigorous Quality Management Systems to ensure every product meets the highest standards.
Plastic Products international Contact Us: info@ppiuk.net www.ppiuk.net +44(0)1279 445 041