Your work nourishes bodies, expands minds and saves lives. Our work helps that happen.
Your work nourishes bodies, expands minds and saves lives. Our work helps that happen.
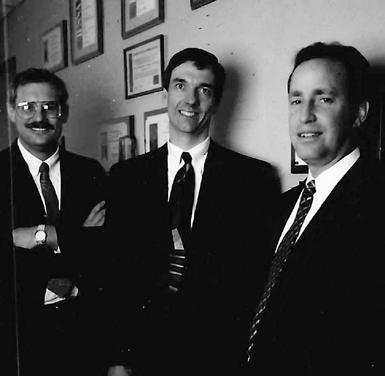
1984
Founded in Kansas City, MO as a highly technical engineering consulting firm
2007
Formed CRB Caribe to serve Puerto Rico market Genentech Oceanside project recognized as ISPE Facility of the Year
Began ownership expansion to employee shareholders
1990
Completed first design-build project; a 100,000 sf facility for Abgenix
2003
Designed first project outside the U.S.
2012
Surpassed 600 employees and earned second ISPE Company of the Year Award
1997
2001 Named ISPE Company of the Year
Formed a dedicated construction services team
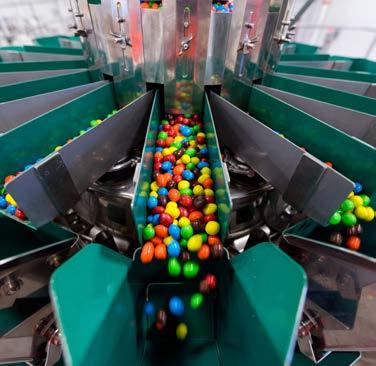
Mars Chocolate North America project recognized as Food Engineering Plant of the Year
2015
Opened first European office in Basel, Switzerland
2018 Surpassed 1,000 employees
Won ISPE Company of the Year Award for the third time
Recognized in ENR’s Top 10 Contractors for Pharmaceuticals, Food + Beverage, and Industrial Process
2022
2023
KBI Biopharma project recognized as Advancing Prefabrication Project of the Year
2024
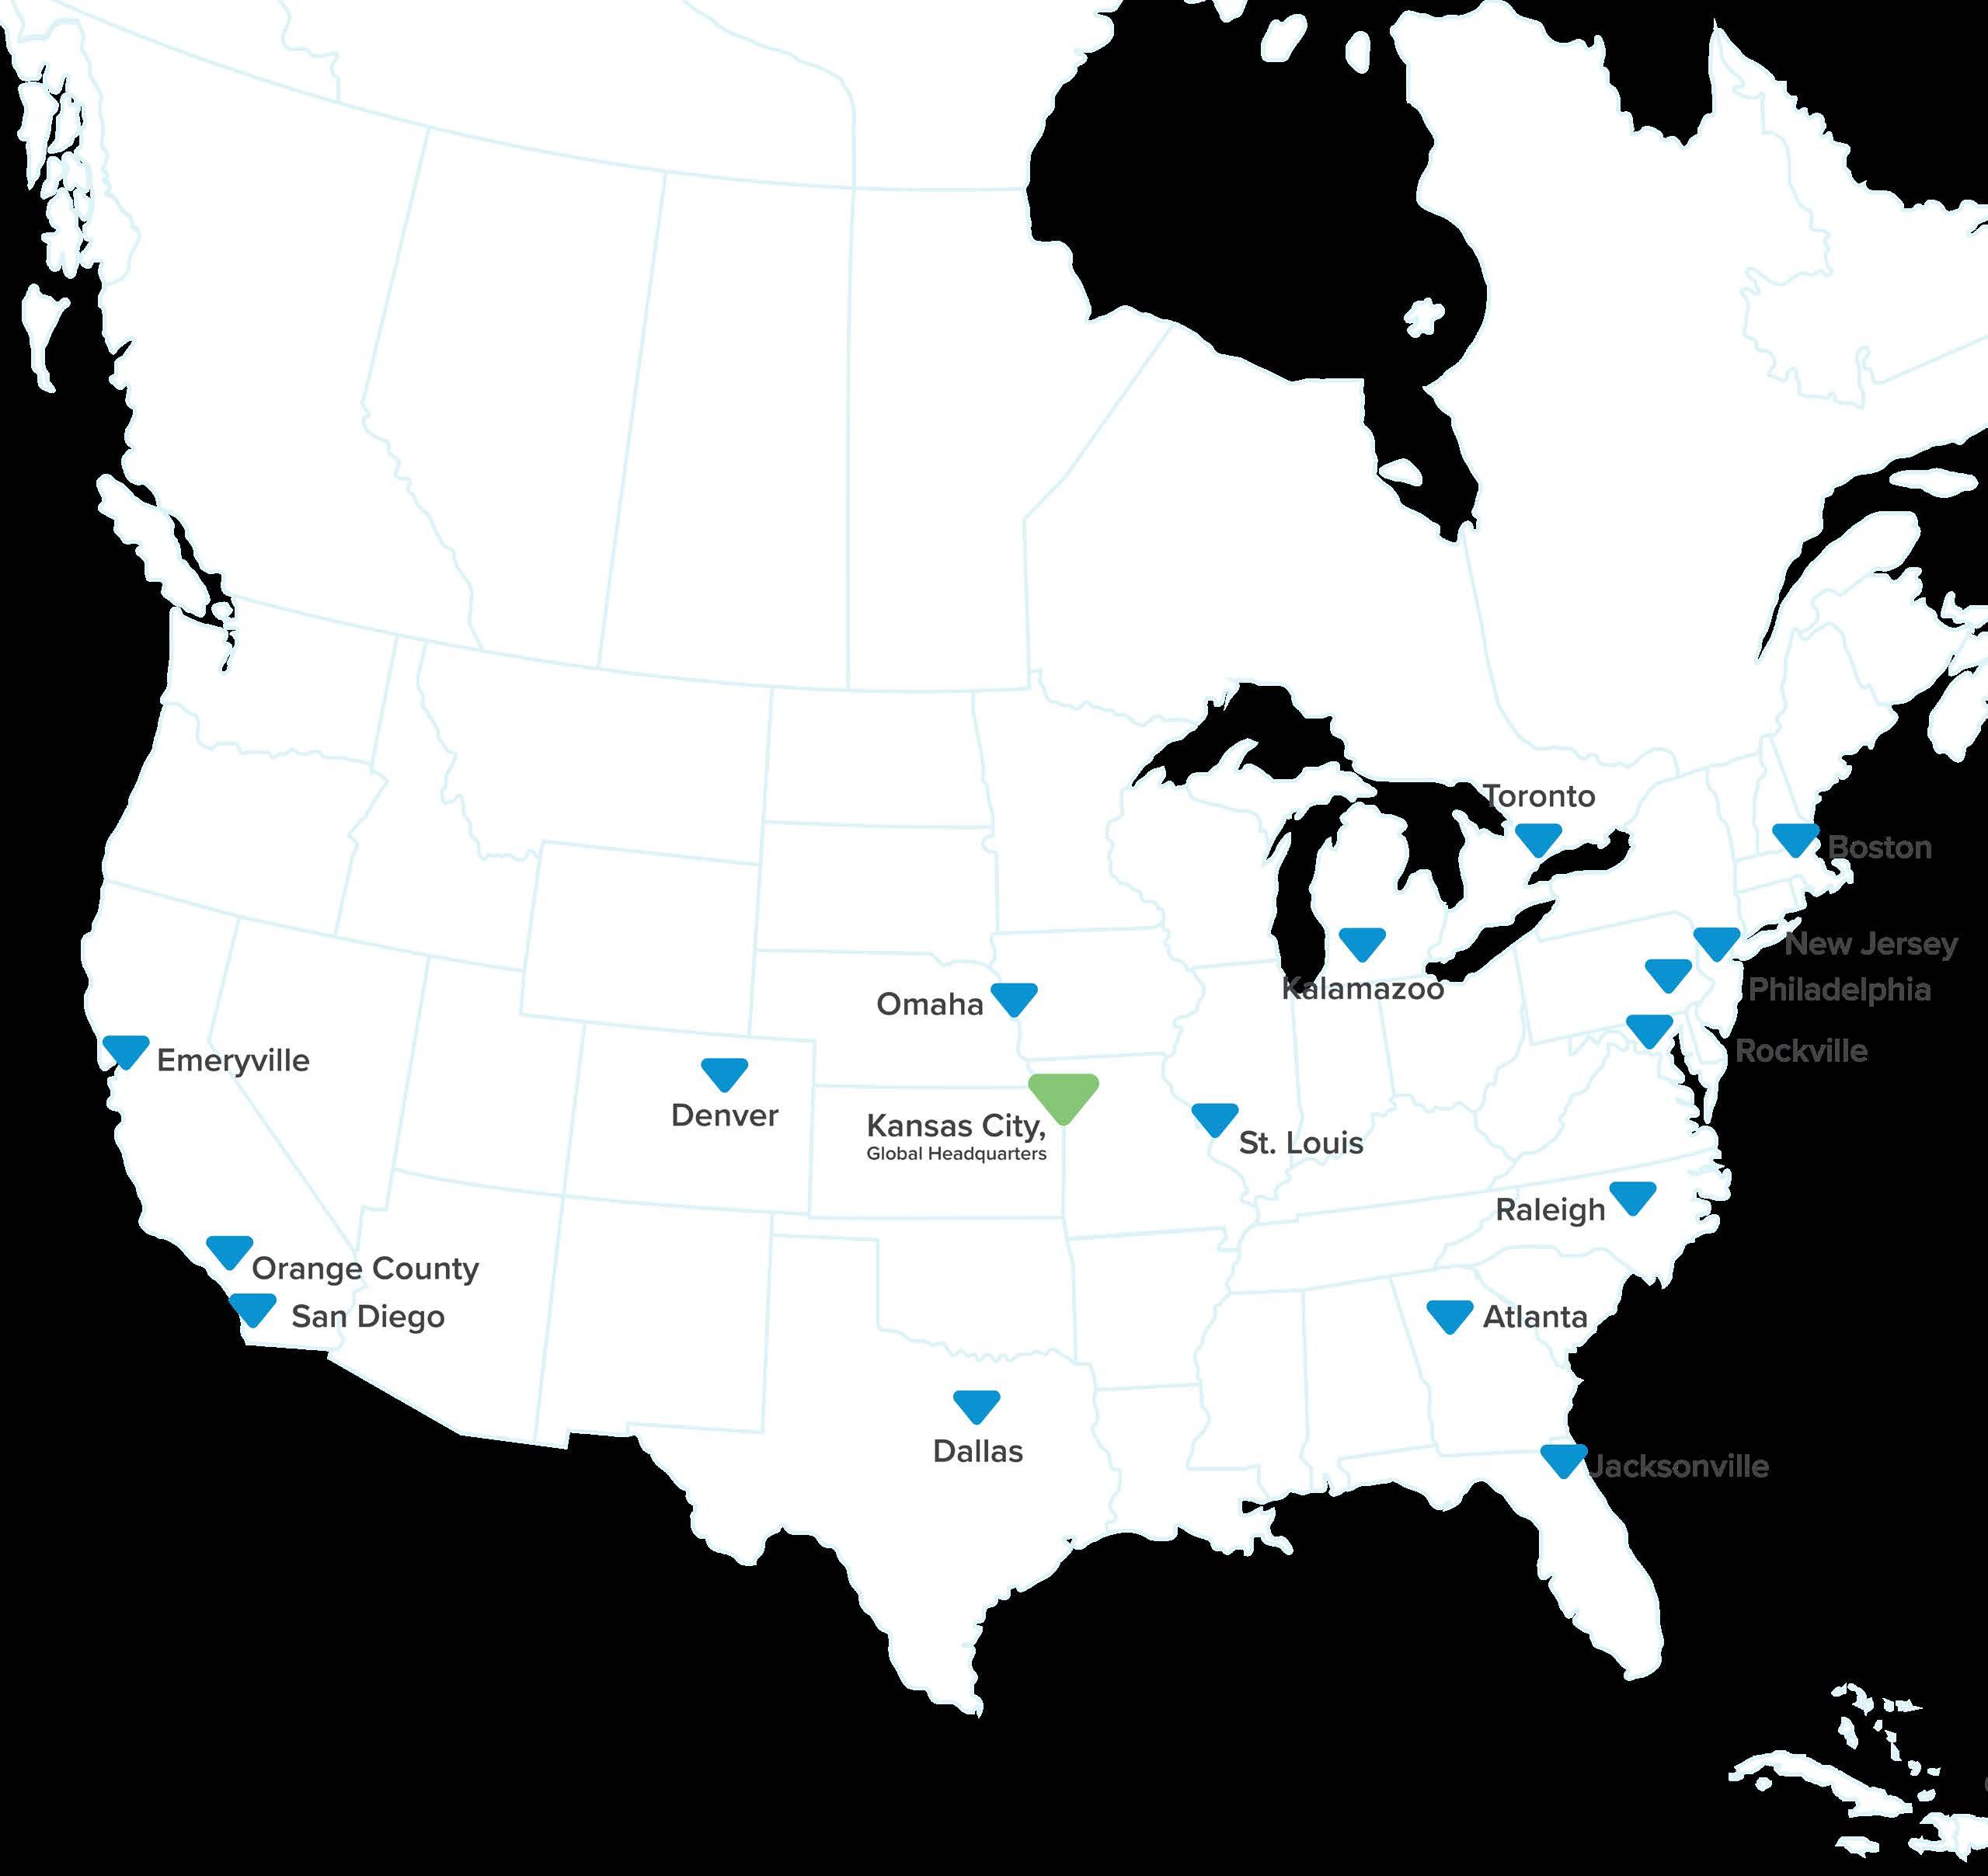
Continued global expansion, reaching 20 office locations
2020
MycoTechnology project recognized as Food Engineering Sustainable Plant of the Year
Supported 20+ COVID-19 response-related projects
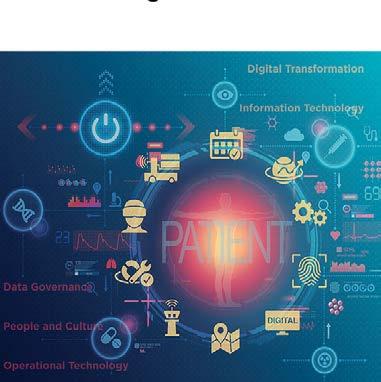
CRB employees contributed to the ISPE Pharma 4.0® Guide, marking 20+ ISPE guides supported by CRB SMEs
Crossed $1B in annual revenue
2026
AstraZeneca facility earned ISPE FOYA, marking the 24th FOYA project supported by CRB
Our vision is just as relevant today as it was when it was written more than 40 years ago. Life sciences companies are increasingly pivoting in response to demand shifts, scientific breakthroughs and technological advances. Food manufacturers are adopting automation, control systems and real-time analytics to improve efficiency and resilience.
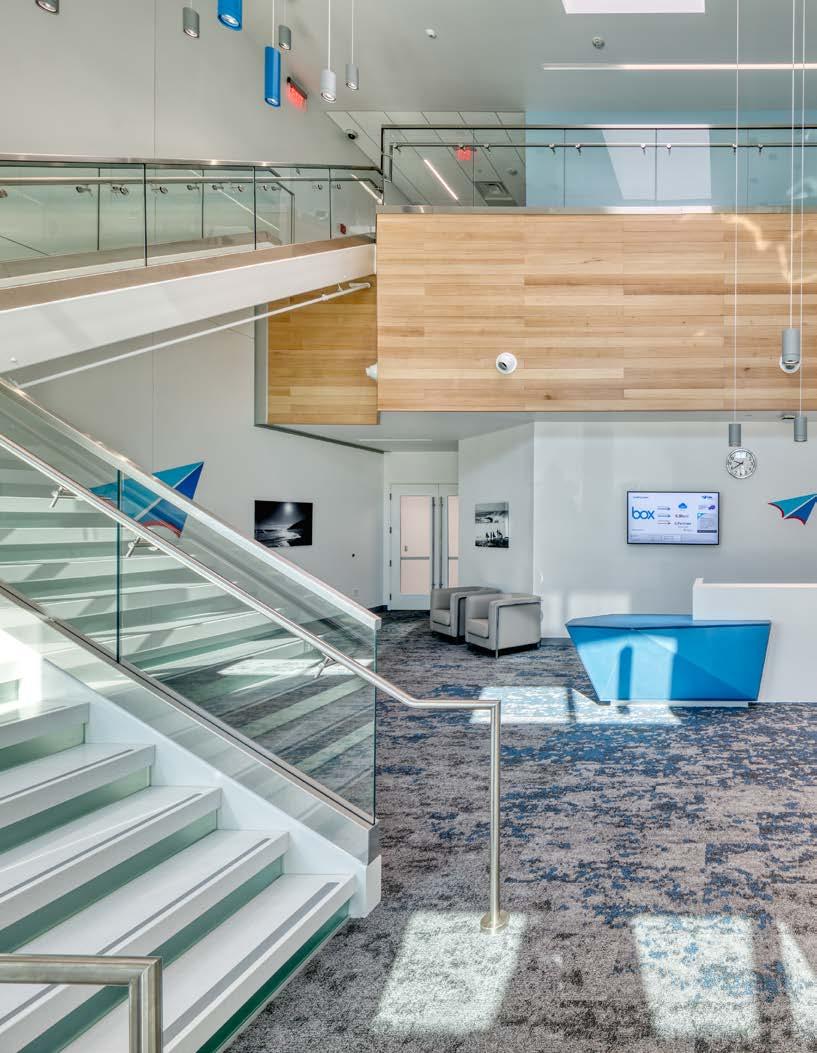
From our first bio-process job to the projects we are executing today, our expertise has grown exponentially along the way. CRB is now a leading provider of sustainable engineering, architecture, construction and consulting solutions to the global life sciences and food & beverage industries. From 21 offices across the United States, Canada and Europe, our professionals provide world-class solutions that drive success and positive change for our clients, our people and our communities.
We are committed to provide best-in-class solutions that drive success and positive change for our clients, our people, and our communities.
We believe that by helping our clients achieve growth and expand their impact, people all over the world can live better lives. Whether it is research and development, manufacturing or warehouse and distribution, CRB is proud to support clients across established markets as well as emerging and adjacent industries.
Life Sciences
Active pharmaceutical ingredients
Aseptic + sterile products
Antibody drug conjugates
Cell + gene therapy
Therapeutic p
Oligonucleotides
Oral solid dosage
Peptides
Plasma-derived therapies
Radiopharmaceuticals
Research and development
RNA therapies
Alternative proteins
Baking + snack
Beverage
Confectionery
Consumer products
Dairy
Dressings + sauces
Ingredients
Nutraceuticals
Pet food
Precision fermentation
Ready-to-eat
From front-end planning to CQV, our team delivers some of the most powerful facilities in the world— those that change people’s lives.
These services represent just a selection of the ways CRB supports our clients across the facility lifecycle. CRB partners with clients to deliver fully integrated projects or to provide targeted services that support specific challenges, timelines or resource needs. Our flexible delivery model allows clients to engage us at any point in the lifecycle and scale support as projects evolve.
Business planning
Capital planning
Facility consolidation/optimization planning
Front-end engineering design
Lab planning
Master planning
Process development
Regulatory strategy support
Site selection and evaluation consulting
Strategic facility planning
Technology transfer planning
Technology evaluation
Architectural design
Automation, instrumentation and controls engineering
Conceptual design
Detailed design
Interior design
MEP engineering
Packaging systems engineering
Process architecture design
Process engineering
Process utility engineering
Structural engineering
These services support ongoing operations and can be engaged at any point in the facility lifecycle.
Control systems integration
Cost of goods evaluation
Equipment procurement
Food safety consulting Industry 4.0 consulting Operations modeling
Operational readiness/CQV Process simulation Regulatory and compliance consulting
Risk assessment
Sustainability consulting
Project delivery
Cost control
Construction administration
Construction management
Estimating
Preconstruction planning
Procurement Safety management
Scheduling
Staff augmentation
Virtual design and construction
Electrical commissioning
Integrated systems testing
Mechanical commissioning
Procedure development
Project information management
Qualification
Turnover execution
Tier certification support
Validation
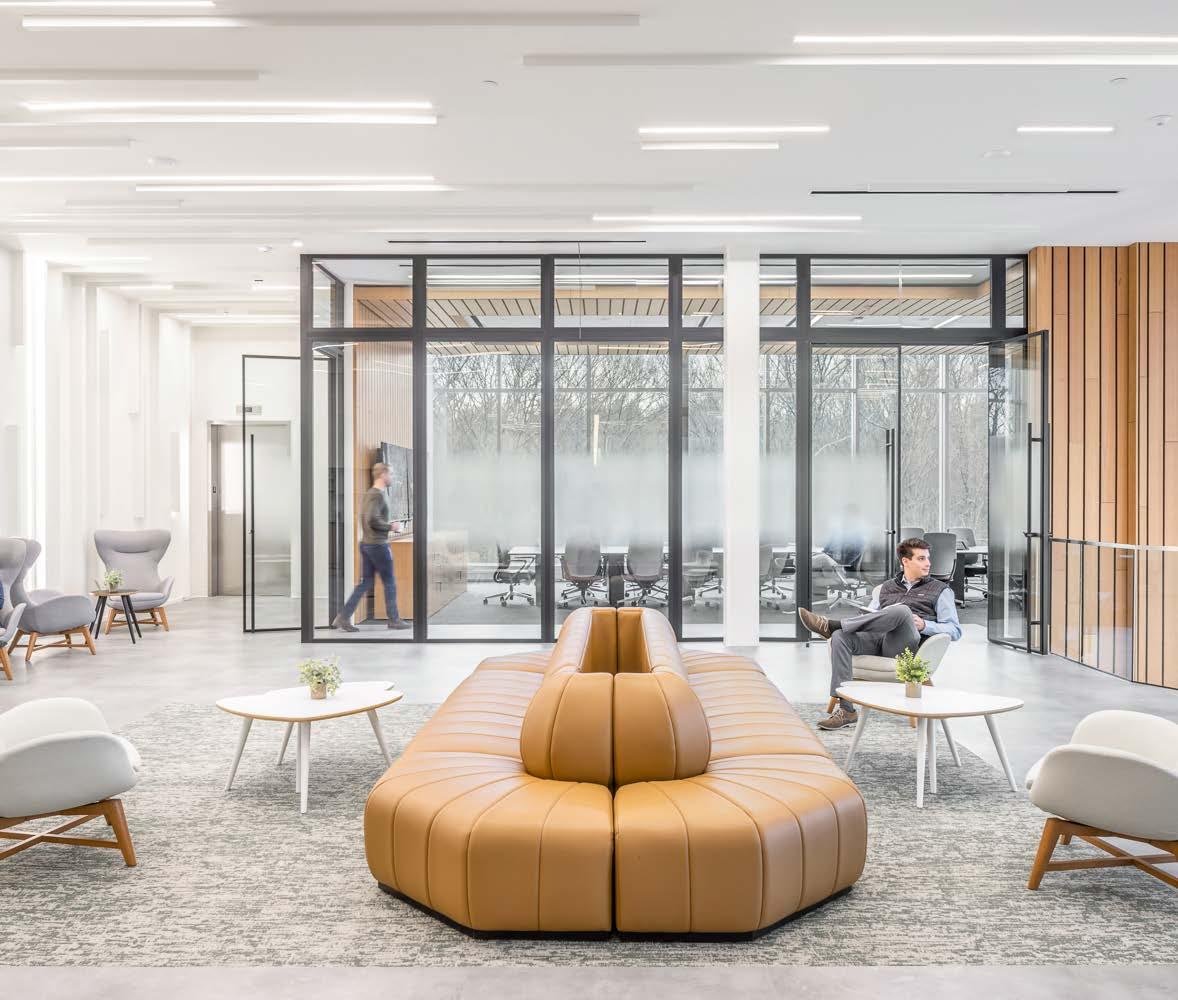
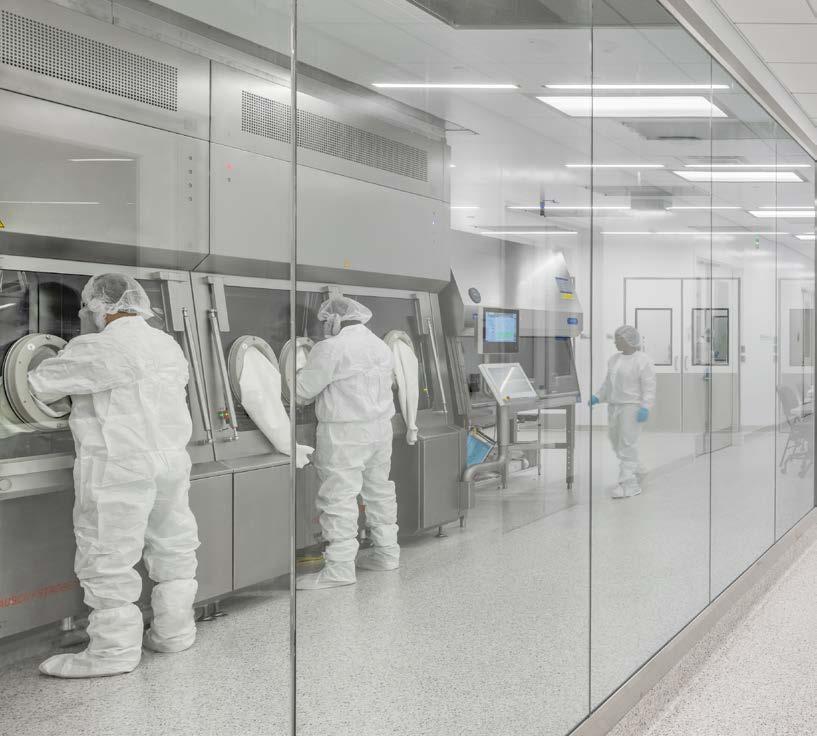
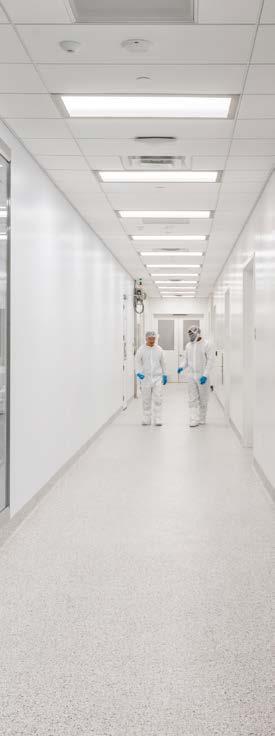
CRB delivered this 110,000 sq ft gene therapy manufacturing facility on time and under budget during the COVID-19 pandemic using an Integrated Project Delivery approach that enhanced collaboration and quality. The fit-for-purpose facility integrates cGMP manufacturing, warehouse, office, and modular mechanical spaces to support rapid scale-up for rare disease therapies. Single-use technology, dynamic modeling, and Pharma 4.0™ tools optimized operations and enabled fast product changeovers. Extensive prefabrication—including a 15,000 sq ft modular mechanical penthouse installed in two weeks— reduced risk, overcame supply chain challenges, and ensured fast track delivery while advancing long-term sustainability.
Front-end planning
Design development
Lifecycle
Co-located drug substance and product operations: Streamlined production, rapid delivery to patients.
Dedication spaces: Mila boardroom honors the first recipient of a personalized therapy.
Patient-centric ethos: Facility design and culture reflect commitment to rare disease patients.
Flexible manufacturing suites: Portable equipment, scalable for multiple gene therapy programs.
“The competition among gene therapy companies for manufacturing capacity at CMOs has become fierce. Building our own facility allows us to decouple from that constraint and gives us flexibility to meet the needs of the patients we serve.”
Tom Lauzon, Senior Vice President, Gene Therapy Manufacturing, Ultragenyx
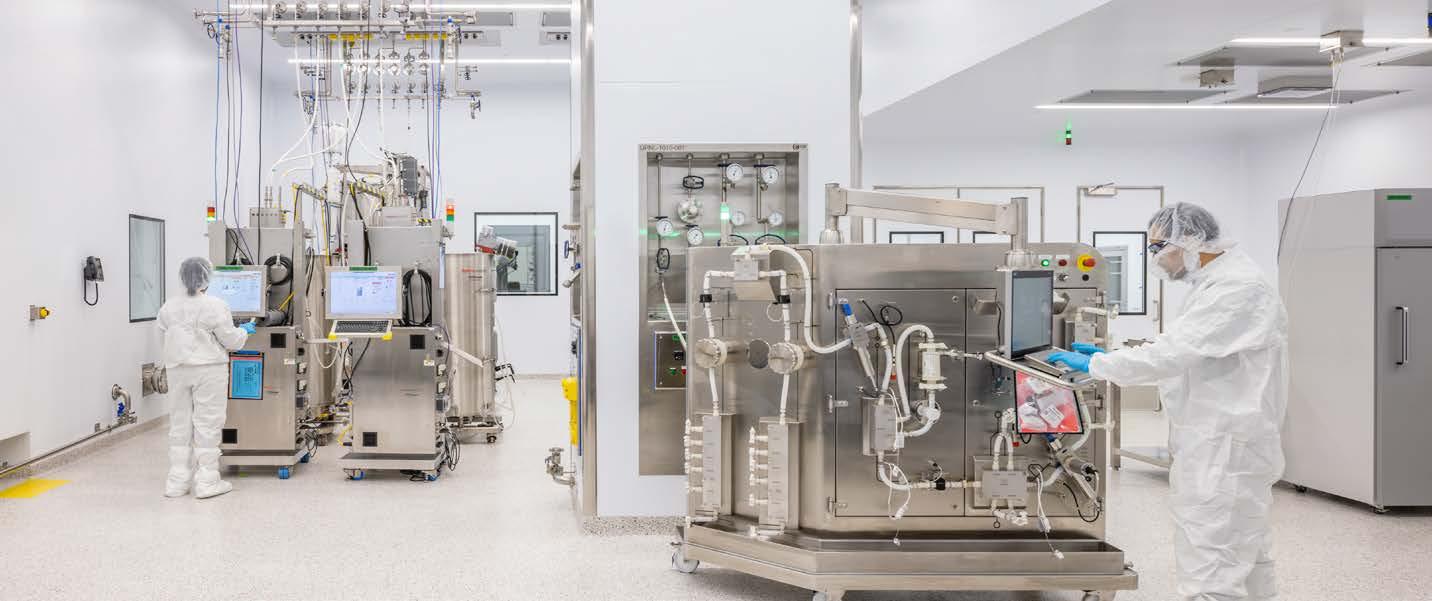
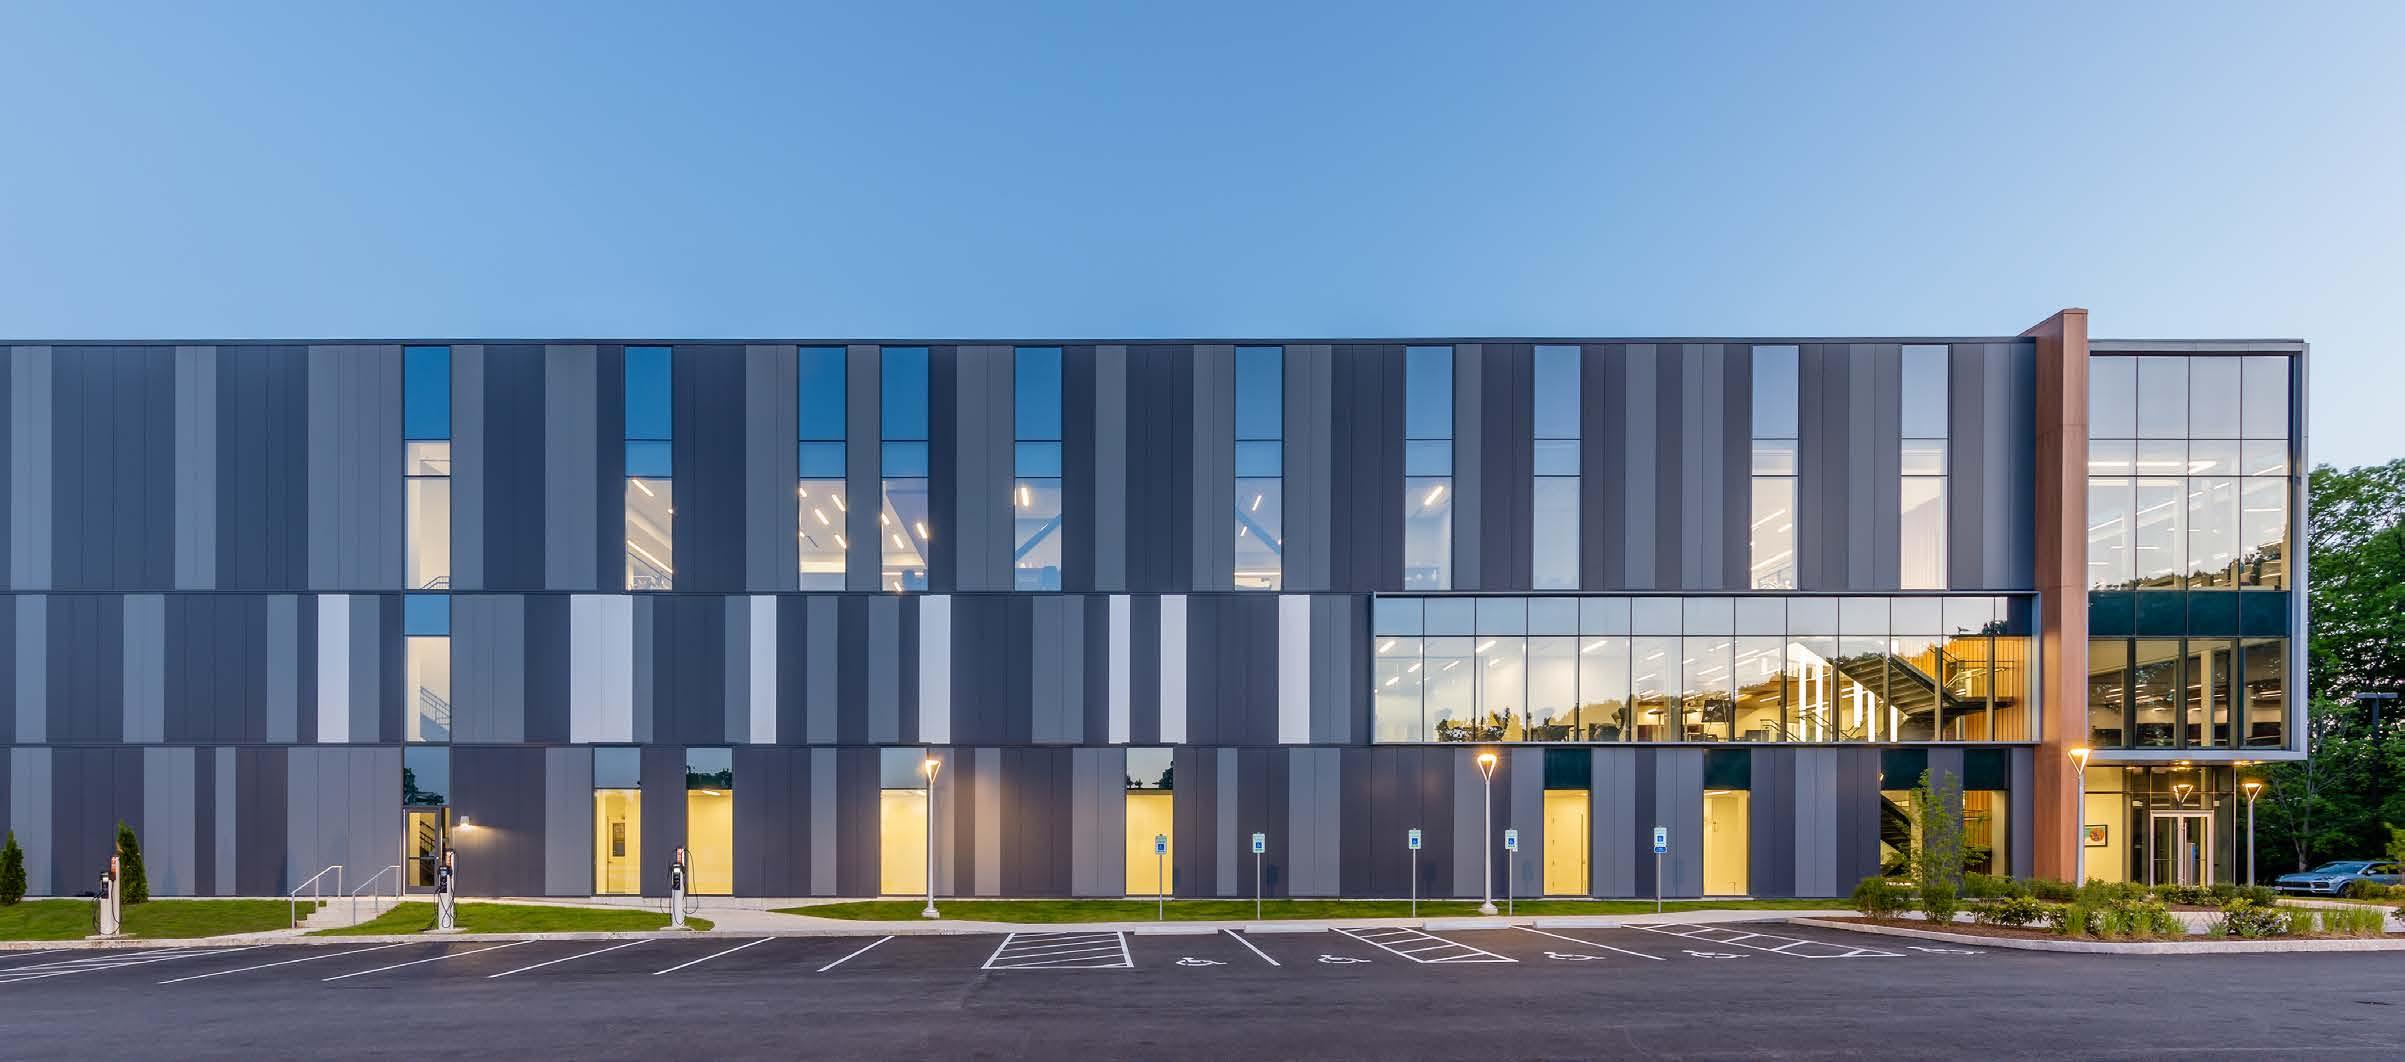
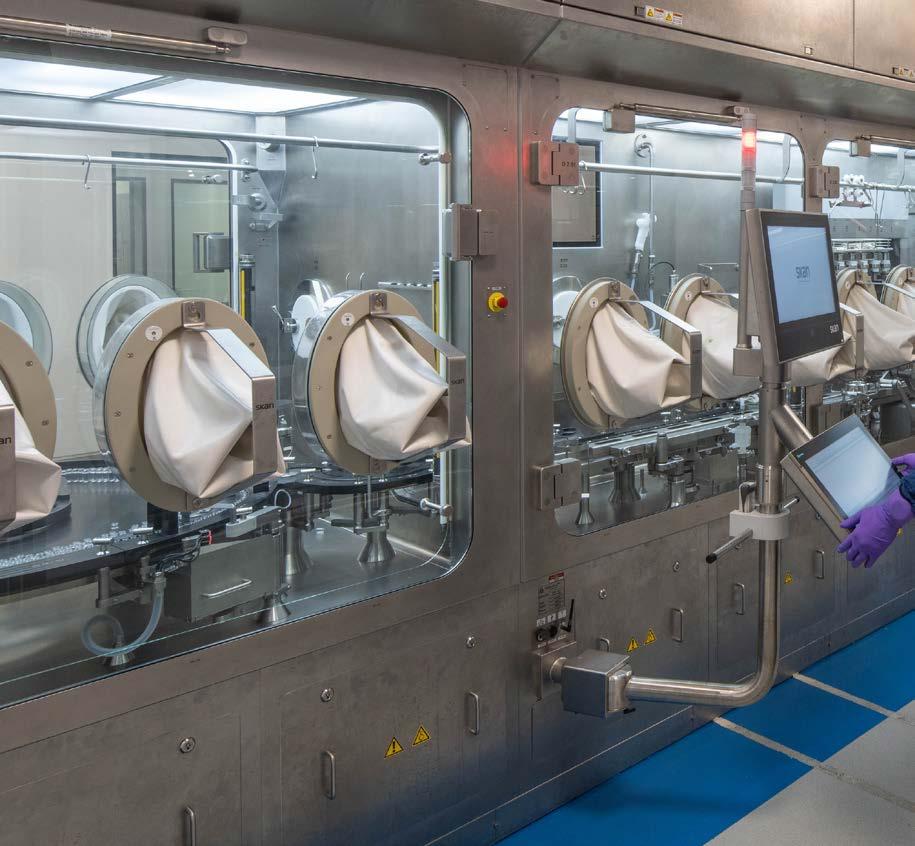
CRB delivered a 200,000 sq ft, EU Annex 1–compliant aseptic fill-finish facility in Bridgeton, Missouri, in just 12 months—four months ahead of schedule—by transforming an aging warehouse into a high-performance injectable manufacturing site. The facility includes six fully segregated modular cleanroom suites with annual capacity exceeding 100 million vials, cartridges, and syringes, integrating sterile fill, device manufacturing, and final assembly under one roof while meeting Annex 1 and DEA Class II–V requirements. Innovative engineering solutions addressed severe height and structural constraints through modular design, offsite prefabrication, and externalized utilities, enabling rapid delivery, efficient operations, and a new benchmark for speed, adaptability, and sustainability.
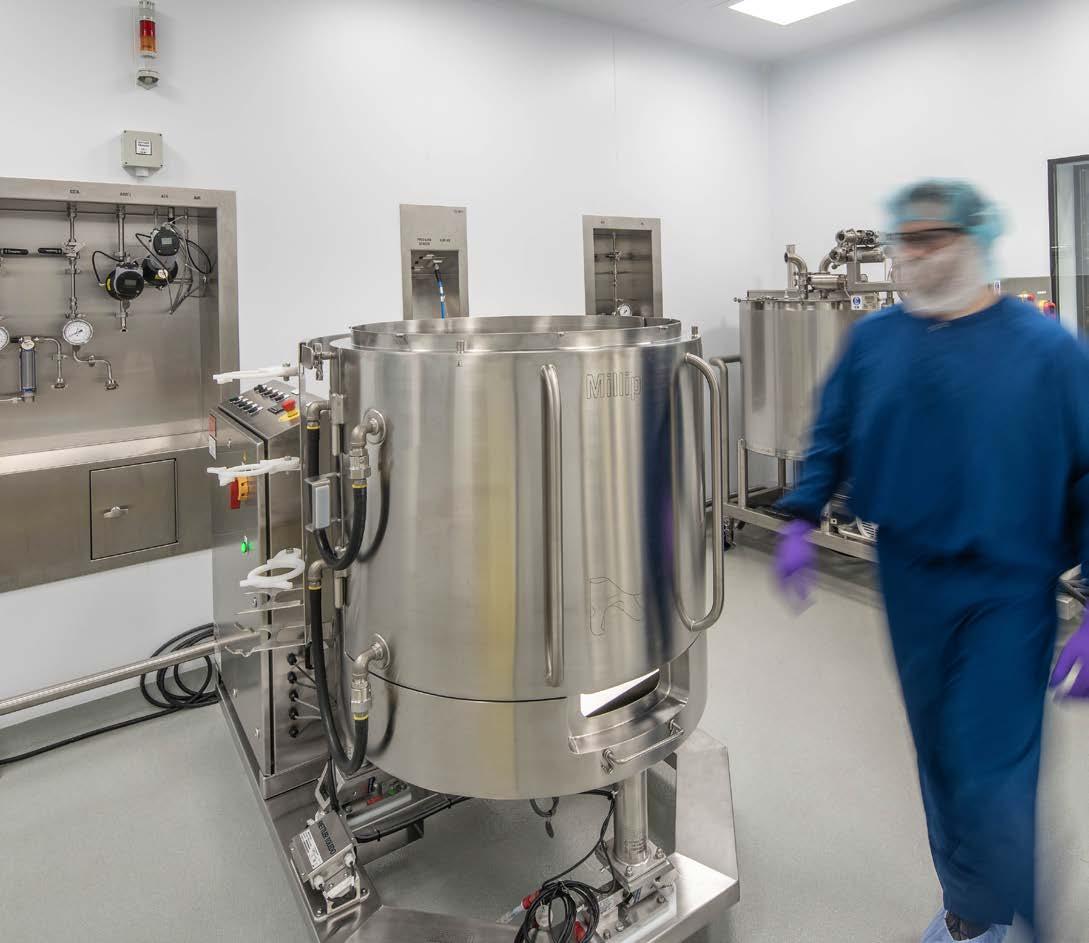
Integrated teaming: A collaborative approach delivered the project ahead of schedule, even with major scope changes. St. Louis, Missouri
Front-end planning
Design development
Project delivery
Advanced technology: Digital twins, VR design and training, and AI-driven SOPs streamlined operations and client engagement.
Modular chillers, closed-loop water systems, and construction waste recycling support sustainability.
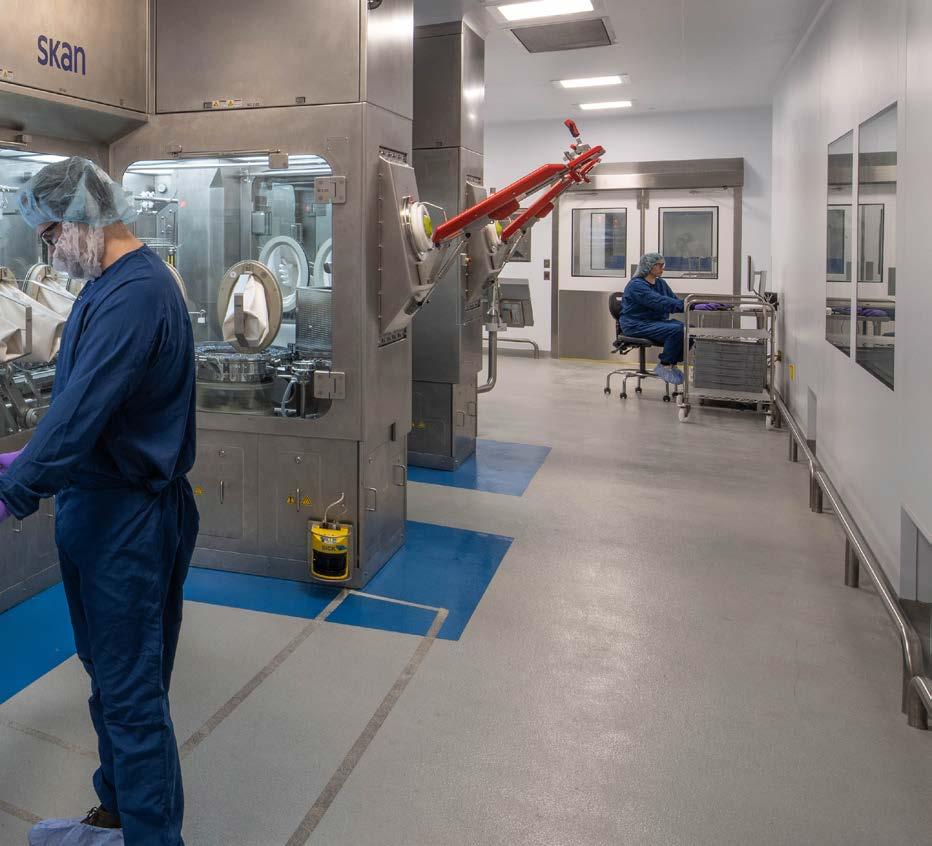
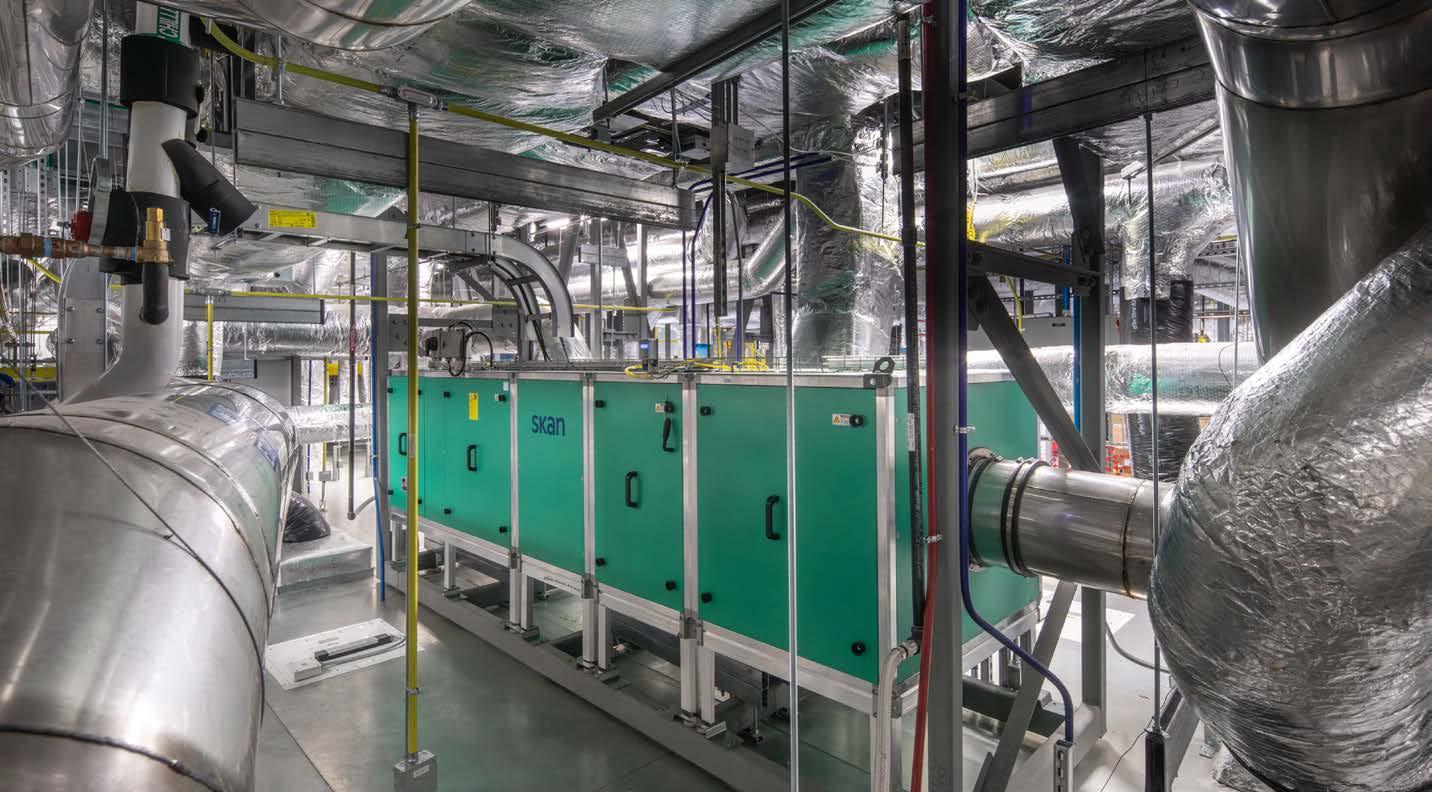
Segregated, modular design: Modular fill suites enable maintenance and upgrades without downtime.
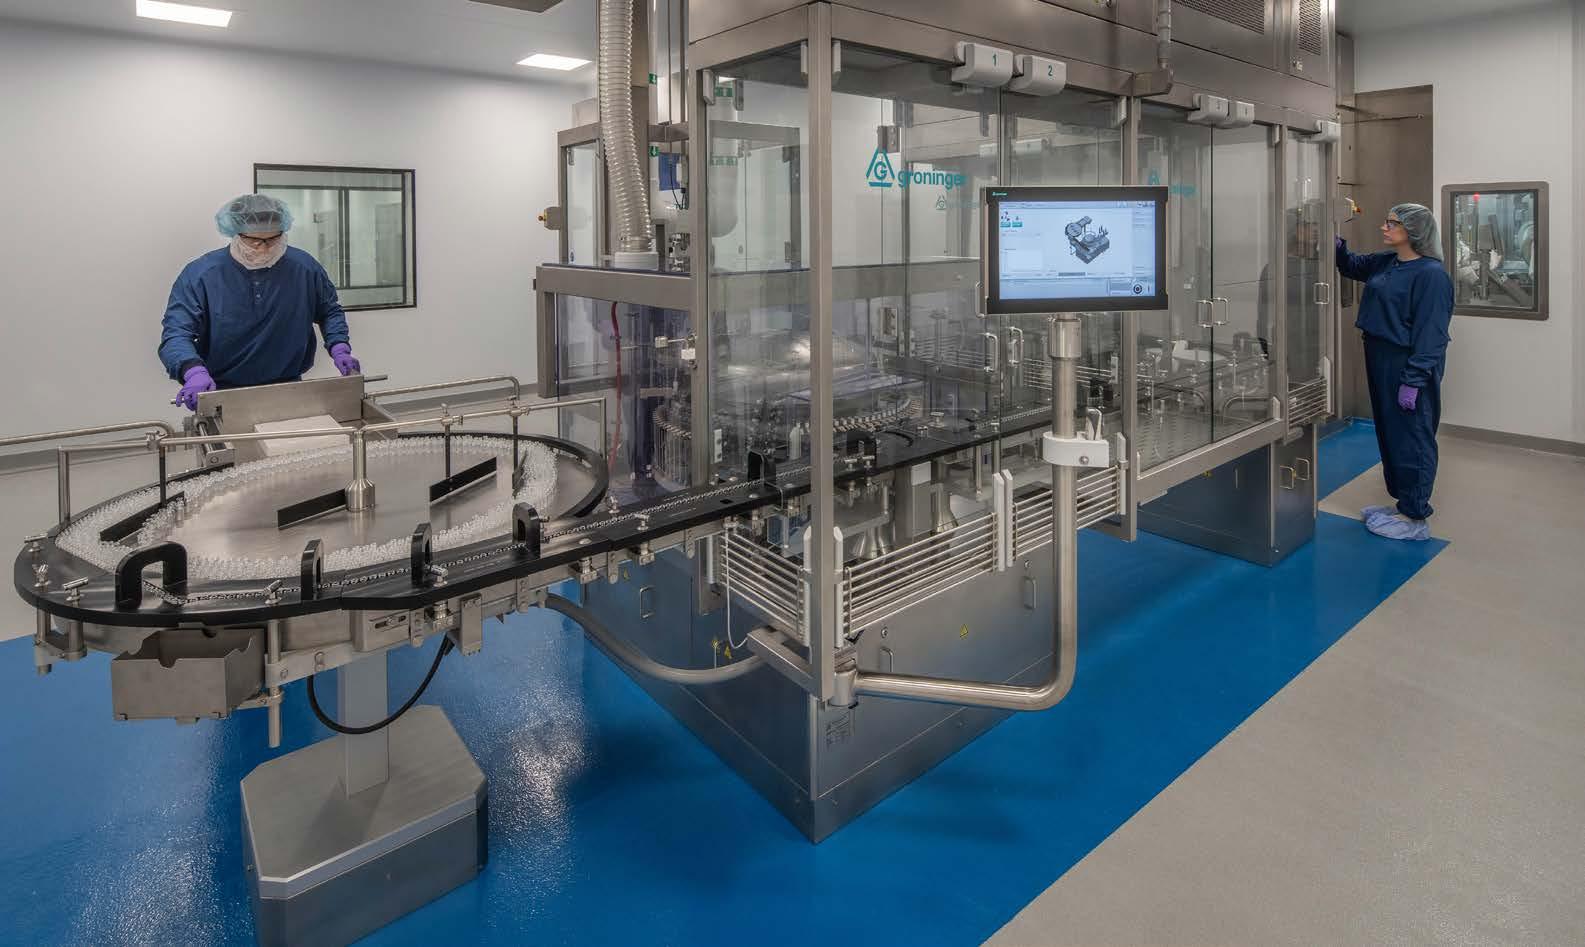
Phased construction: Prefabricated cleanroom panels and pipe racks supported phased delivery and future expansion.
“The opportunity to design a leading facility from the ground up doesn’t come often in one’s career.
Starting with a blank sheet of paper allowed us to build our Bridgeton facility with a strategic eye on future investments.”
Ron Perry, Vice President, STL Operations, Kindeva
Delano, Minnesota
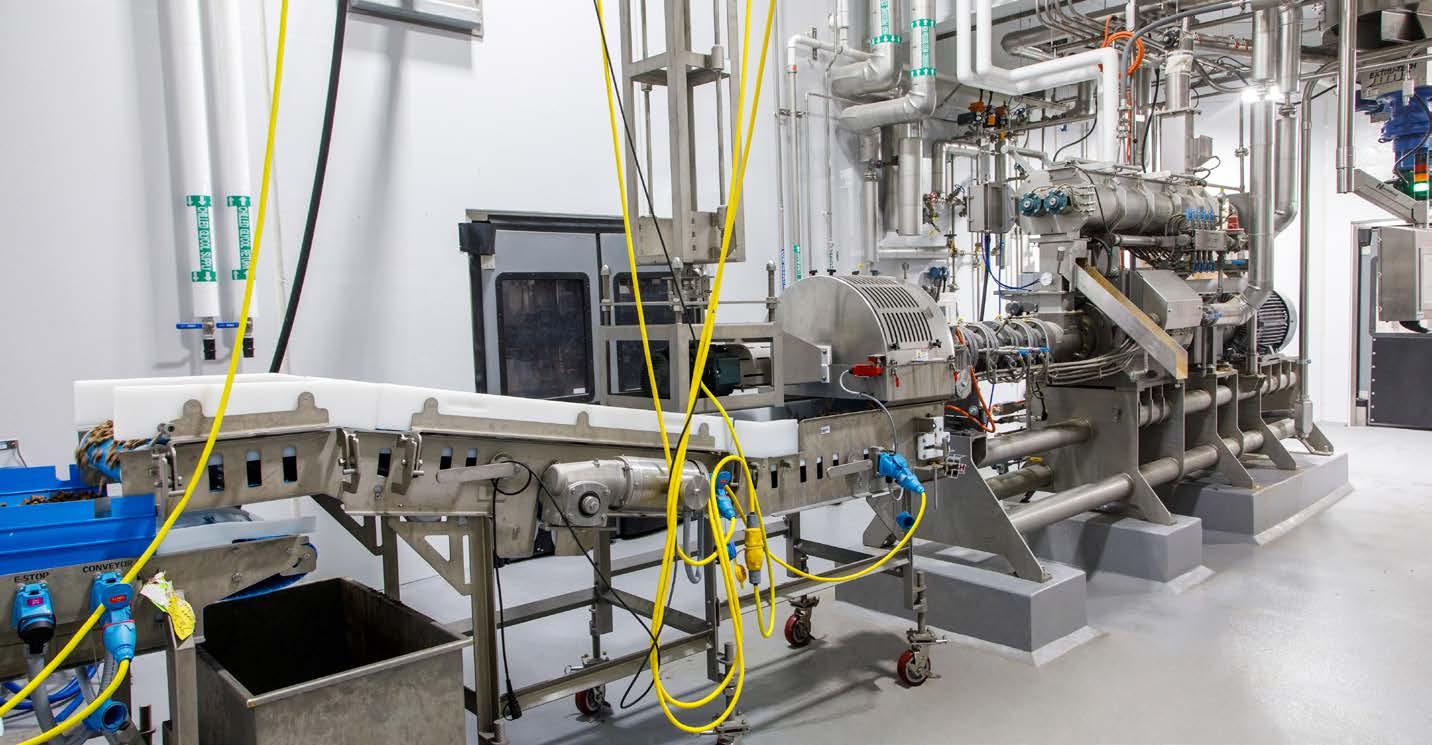
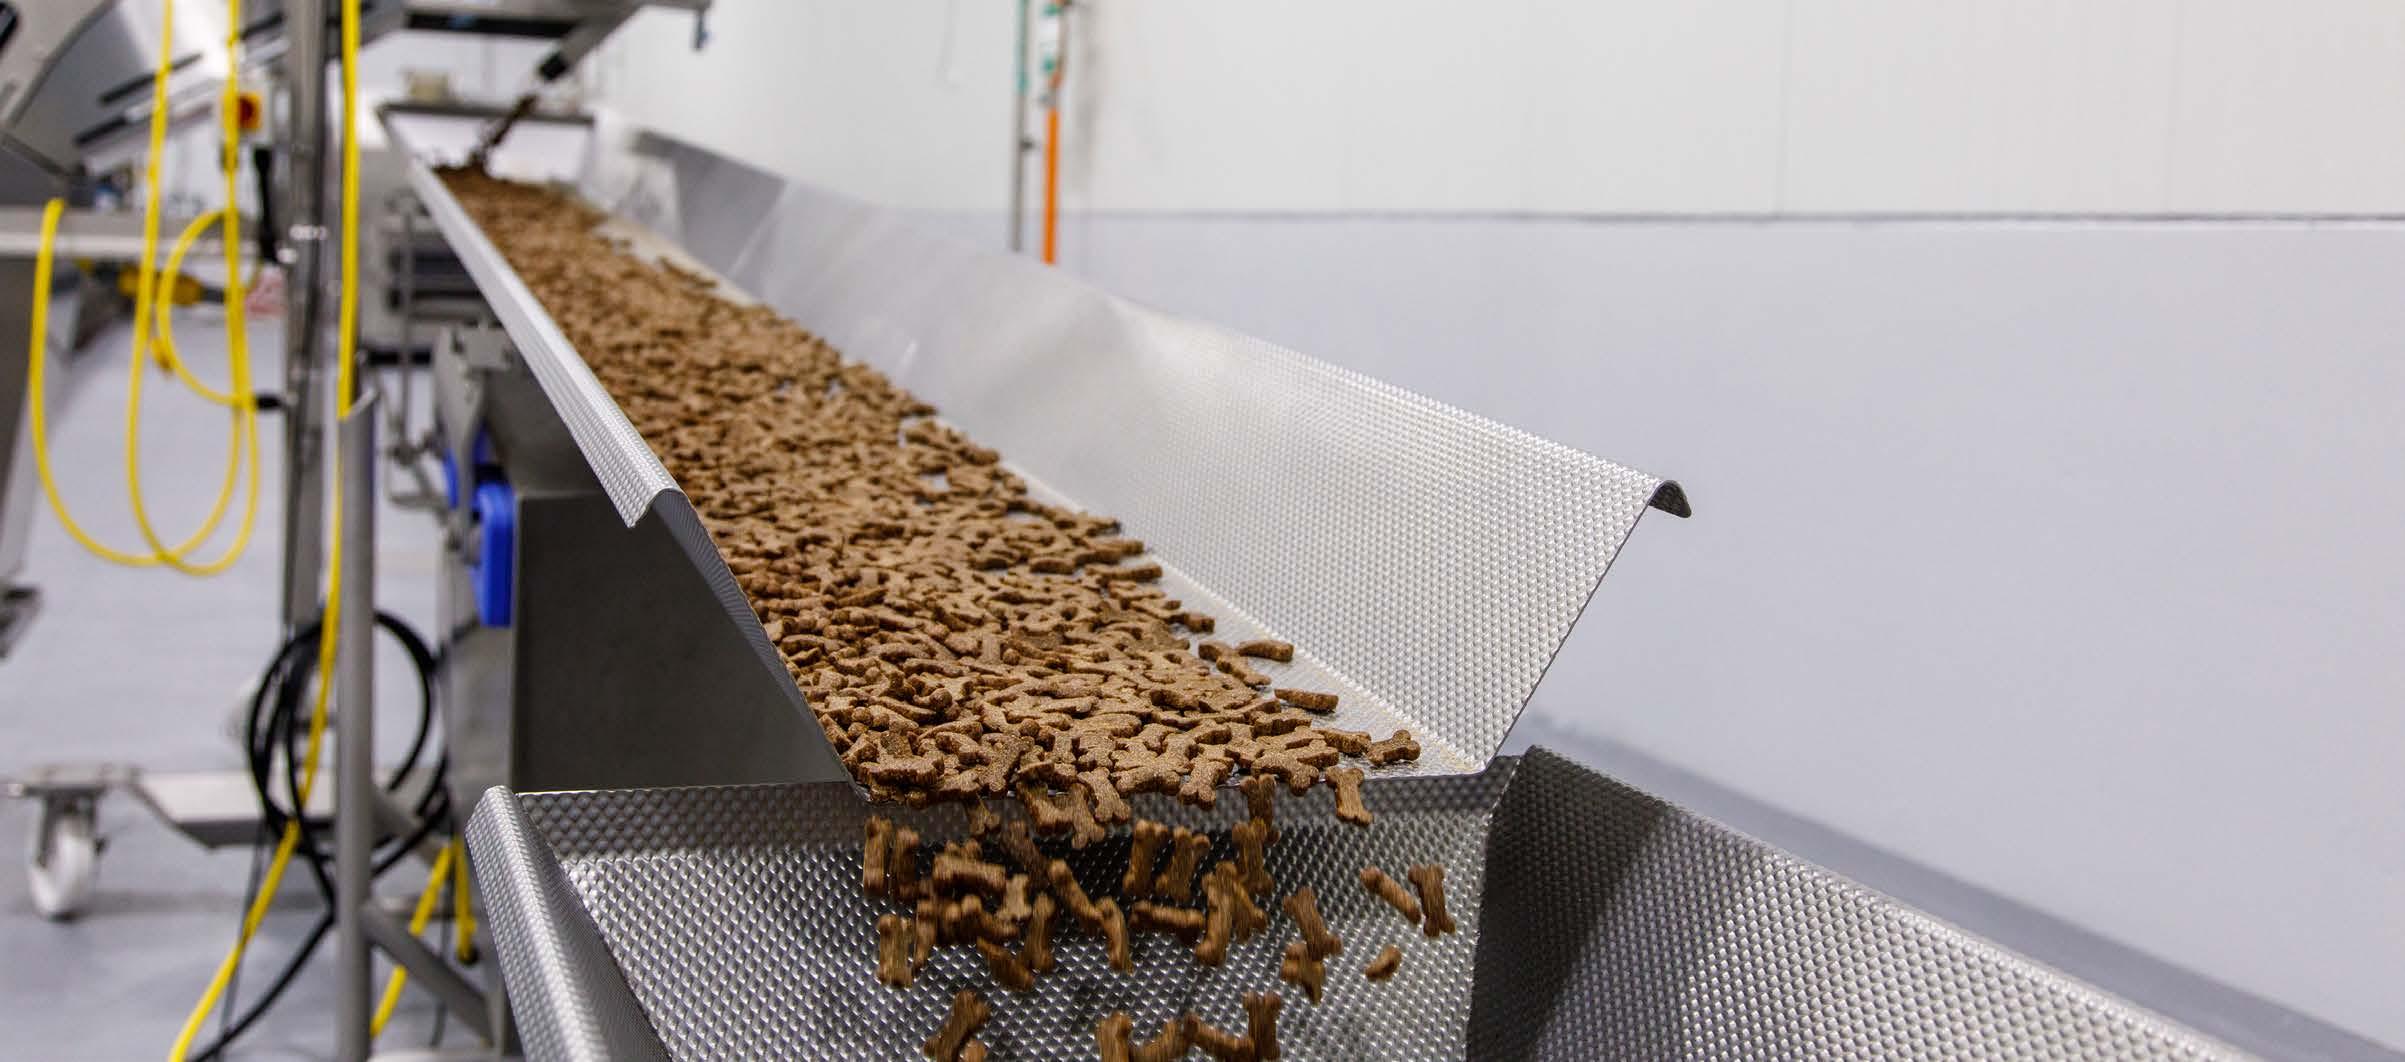
Tuffy’s Pet Treats, part of KLN Family Brands, partnered with CRB to deliver a $65 million, 173,500 sq ft greenfield manufacturing facility in Delano, Minnesota, designed for high throughput, flexible pet treat production. Engineered to achieve 9,000 lbs/hr while supporting rapid changeovers from small batch to large-scale runs, the facility integrates adaptable infrastructure and utilities to enable future expansion and continuous innovation. Designed to biopharmaceutical level food safety standards, the plant features strict pre and post kill segregation, controlled production rooms, cleanable and crevice free surfaces, automated high risk processes, and a walkable interstitial ceiling that allows maintenance outside production areas. Achieving Green Globes certification, the facility reflects KLN’s commitment to safety, sustainability and long-term operational excellence.
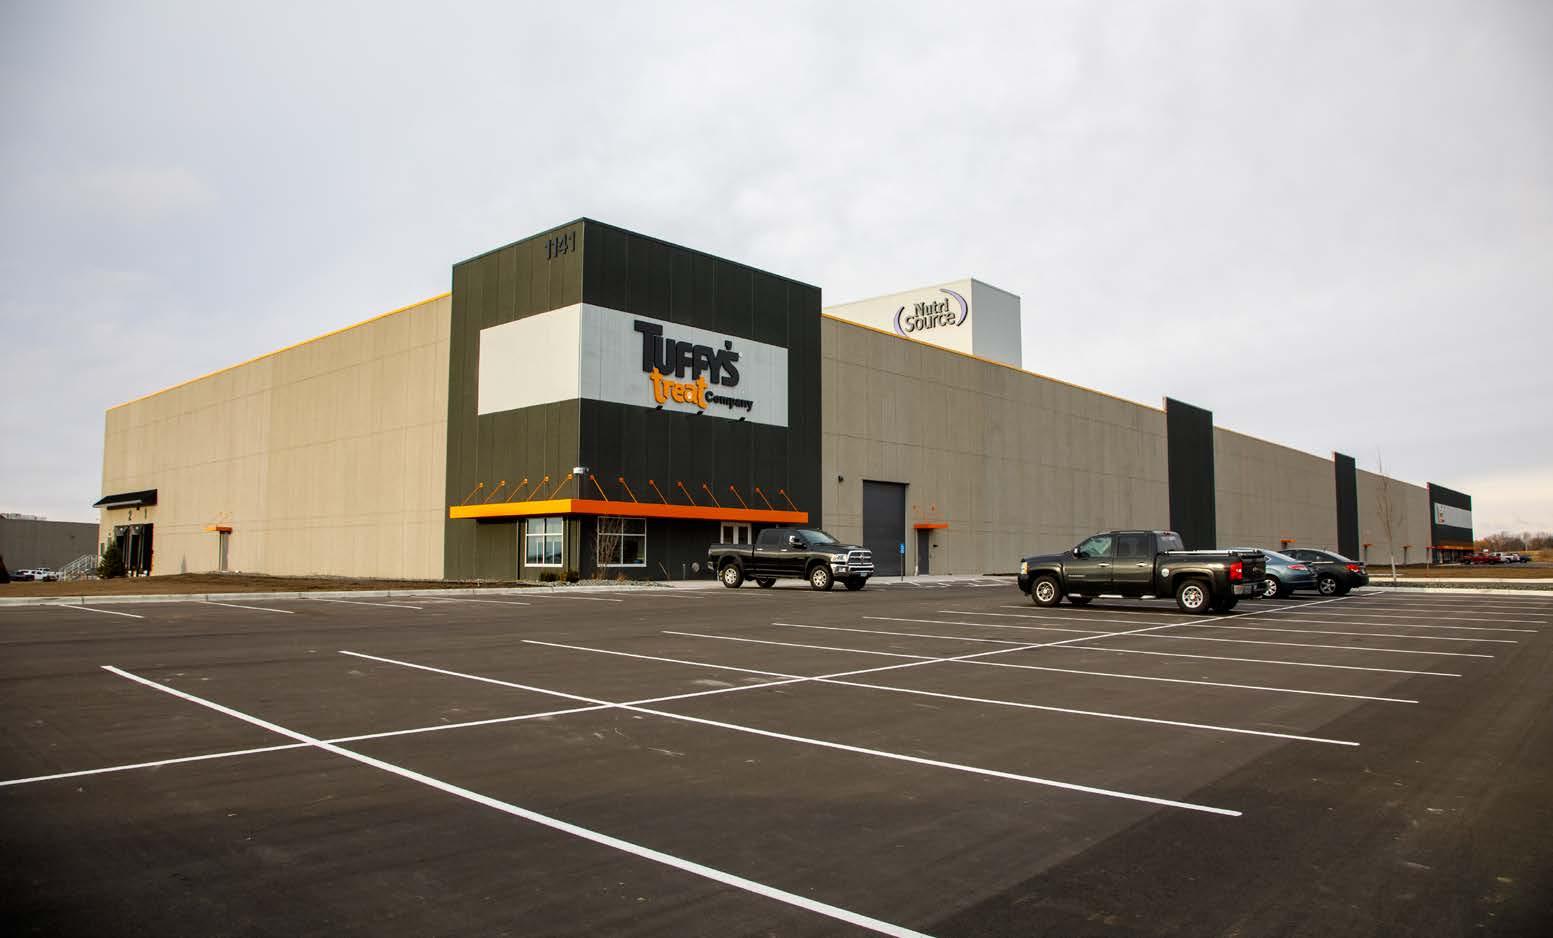
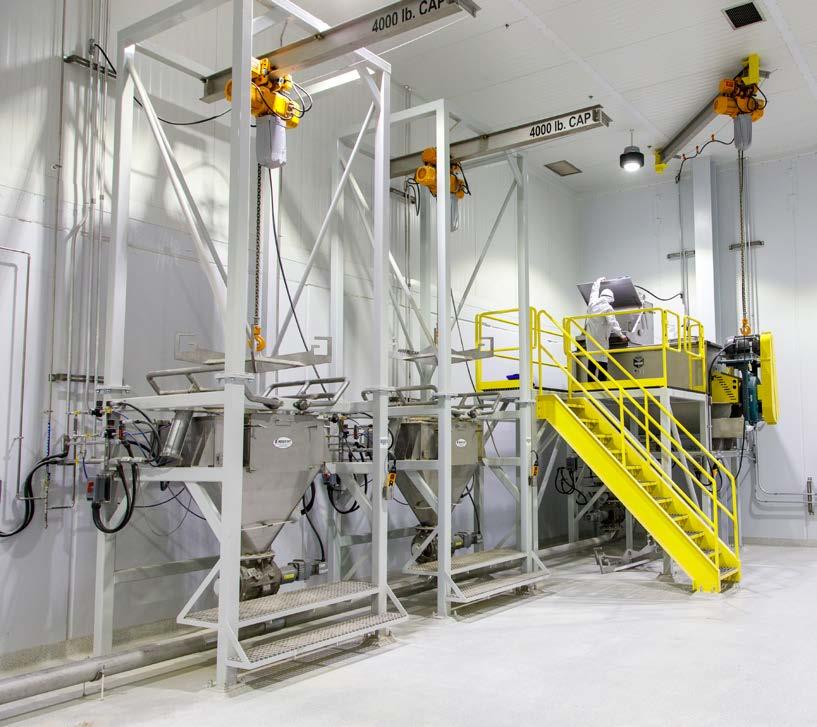
Sustainability and community impact: Energy-efficient systems, employee initiatives, and charitable programs reinforce sustainability and community impact. Design
“At any point, it would’ve been easy for Tuffy’s to say, ‘That’s good enough, we’re satisfied.’ But that’s not Tuffy’s. In four decades, I’ve never seen them stand still.”
Melanie Foss, 40-year employee, Tuffy’s
Built for rapid changeover:
Supports both small and mega production runs.
Future-ready facility design:
Designed with adaptable equipment to enable long-term growth.
CRB designed and fitted out an existing shell to deliver three production suites for large-scale COVID-19 mRNA vaccine manufacturing for a global CDMO. Through close collaboration with stakeholders and vendors, the first GMP suite was operational just eight months after kickoff. CRB translated evolving process requirements into flexible layouts, enabling early procurement of longlead equipment—delivered in under six months. During concept and detailed design, CRB partnered with the EPCM team on 3D modeling, process and utilities design, and coordination to support parallel construction. CRB also supported commissioning, qualification, and startup alongside the client’s CQV team.
Rapid speed-to-market:
Production in the first suite just eight months after kickoff
“Thank
you for your commitment...
I don’t have to explain to anyone what all this work is for!”
Project Leadership, Confidential Client
Front-end planning
Design development
Startup
Flexible spaces:
Adaptable layouts allowed for accelerated procurement.
Multi-national collaboration:
Our local team in Basel, Switzerland served as the boots on the ground through all phases of the project supported by our team in the United States.
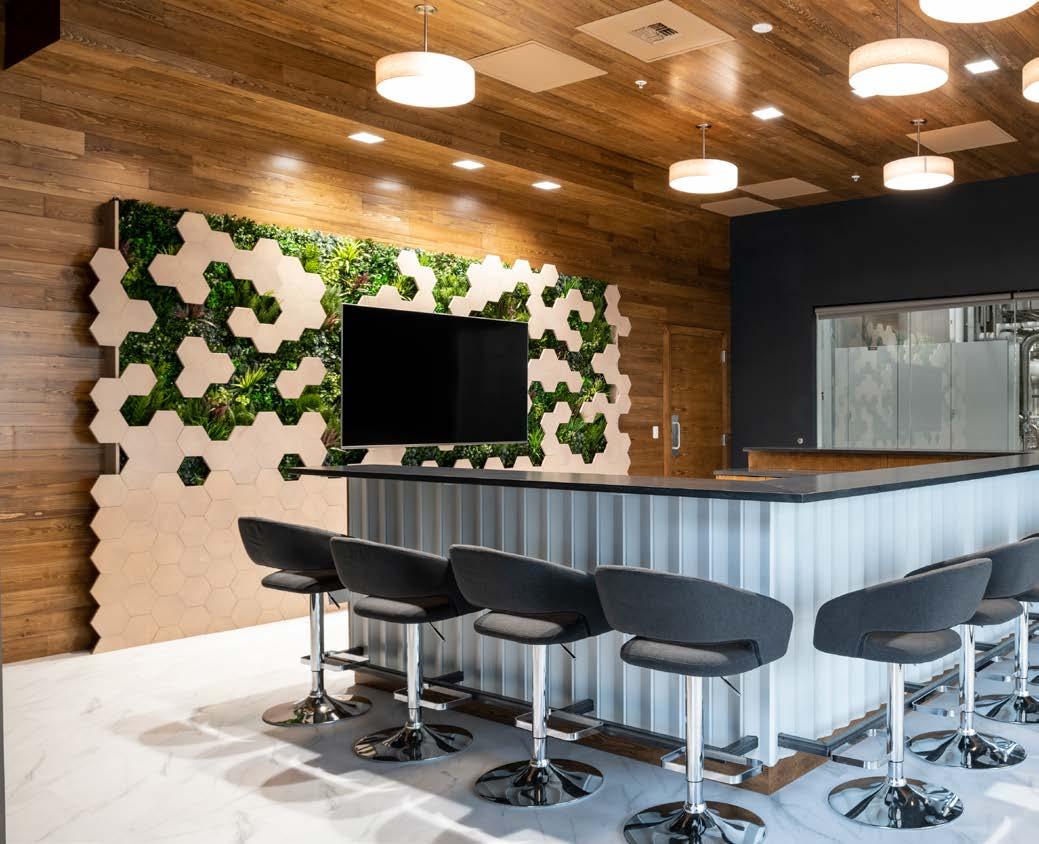
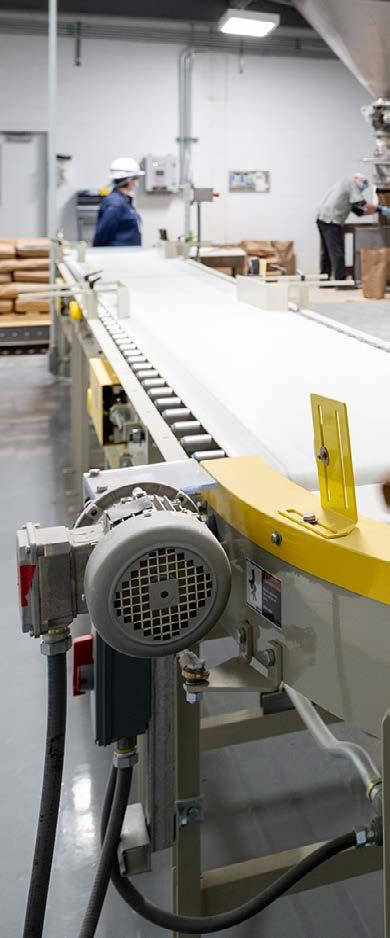
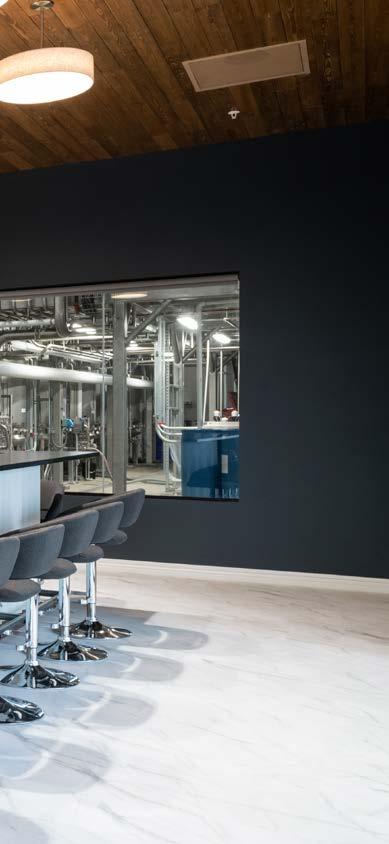
CRB partnered with MycoTechnology to design and build a first-of-its-kind headquarters and fermentation plant that redefines sustainable food production. This award-winning facility supports MycoTechnology’s mission to create healthier, cleaner-tasting plant-based proteins through innovative mushroom fermentation.
Design development
Project delivery
Lifecycle
Built for excellence:
Integrated R&D, QC, and testing spaces with compliant hazardous storage ensure consistent safety and quality.
Sustainability at scale:
Annual water use is reduced by 1.26 million gallons through climate-responsive cooling strategies.
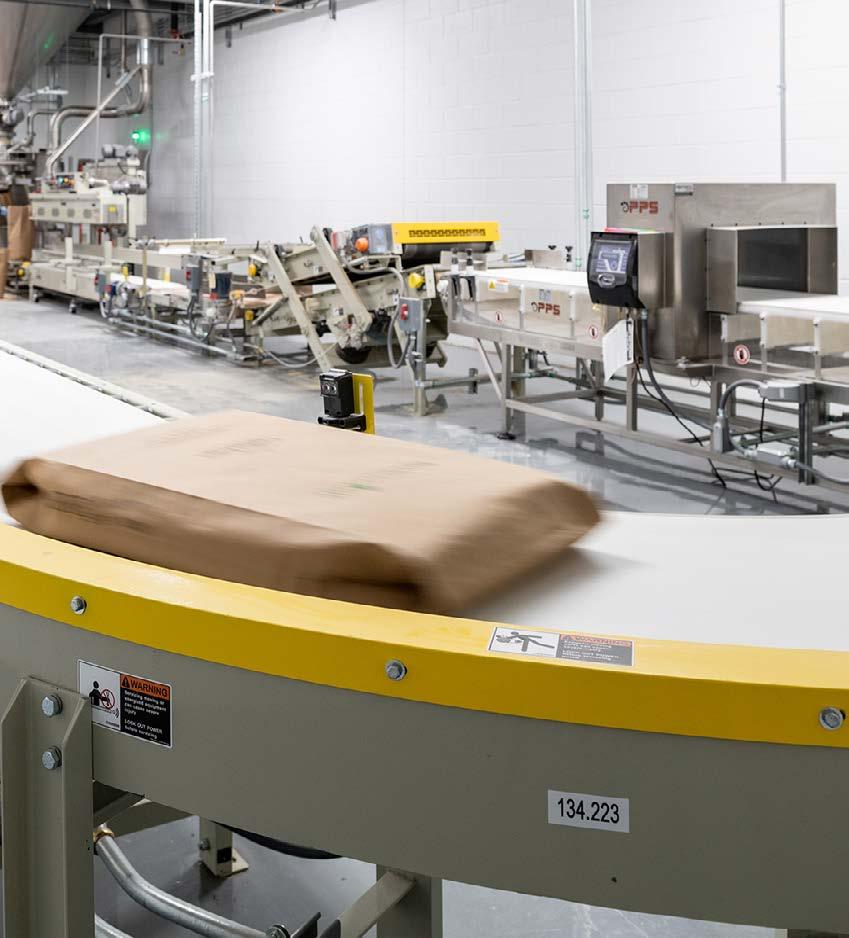
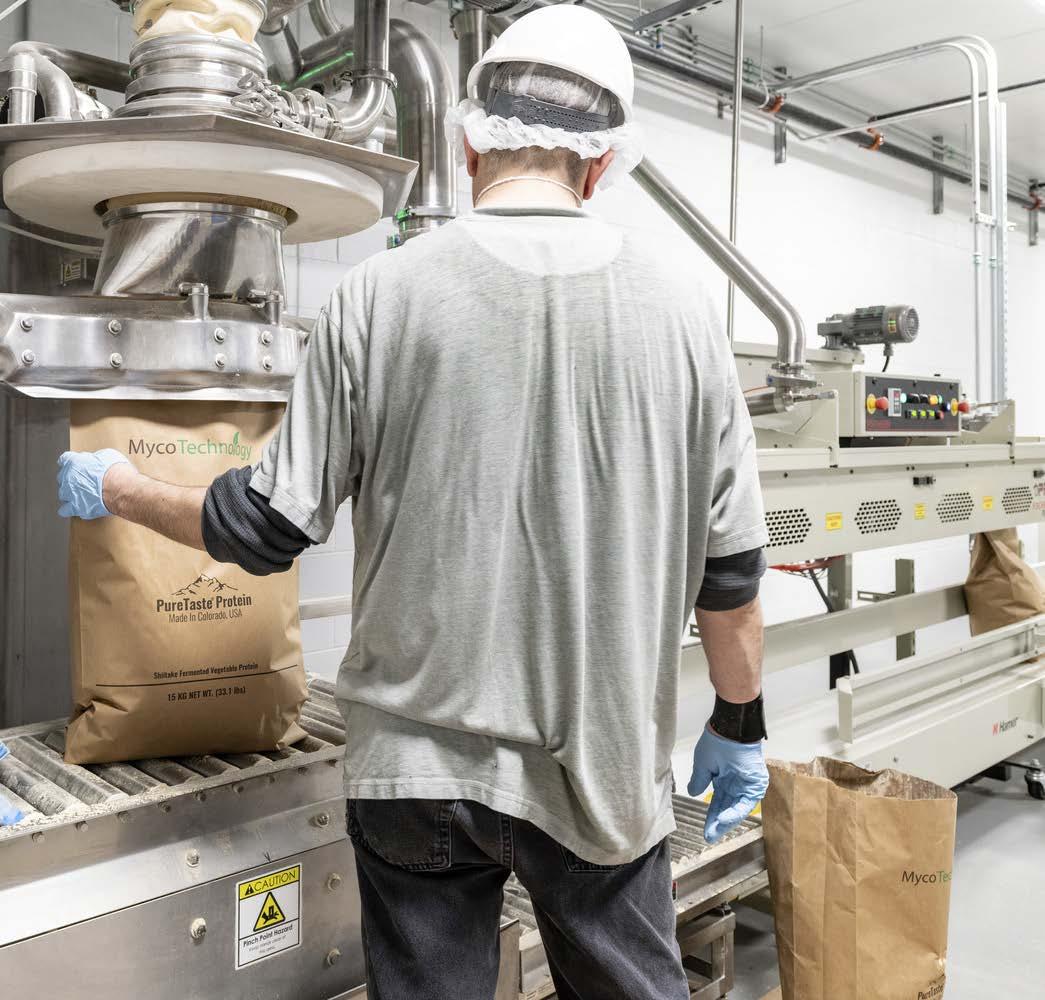
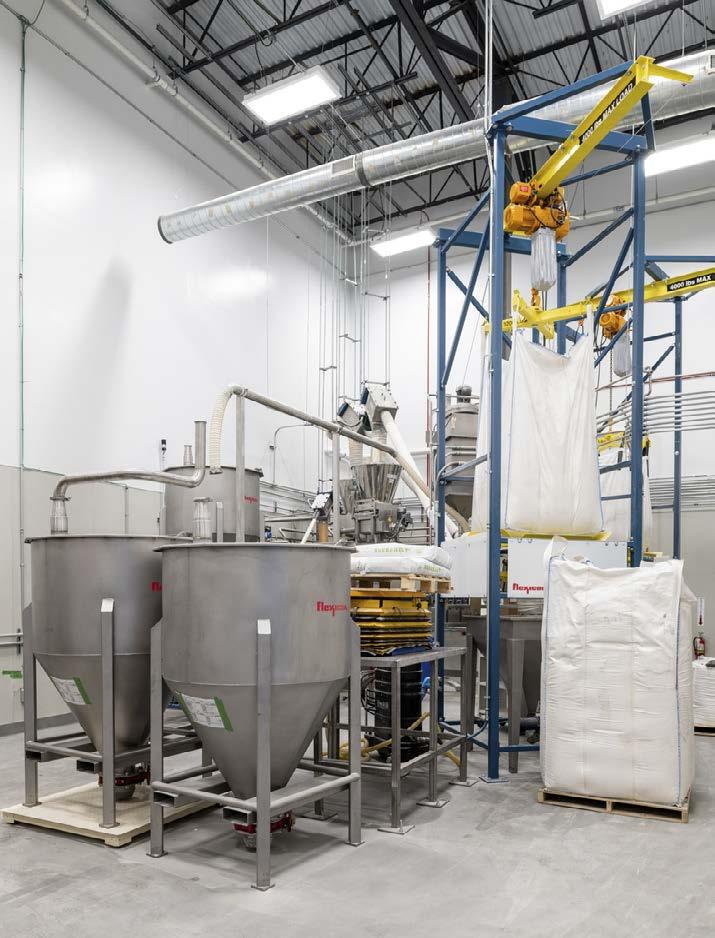
Efficient by design: Vertical production optimizes space utilization, improving efficiency and lowering carbon impact.
Enhanced fermentation: Proprietary shiitake fermentation enhances plant protein quality, enabling 4,000 metric tons of annual FermentIQ™ production.
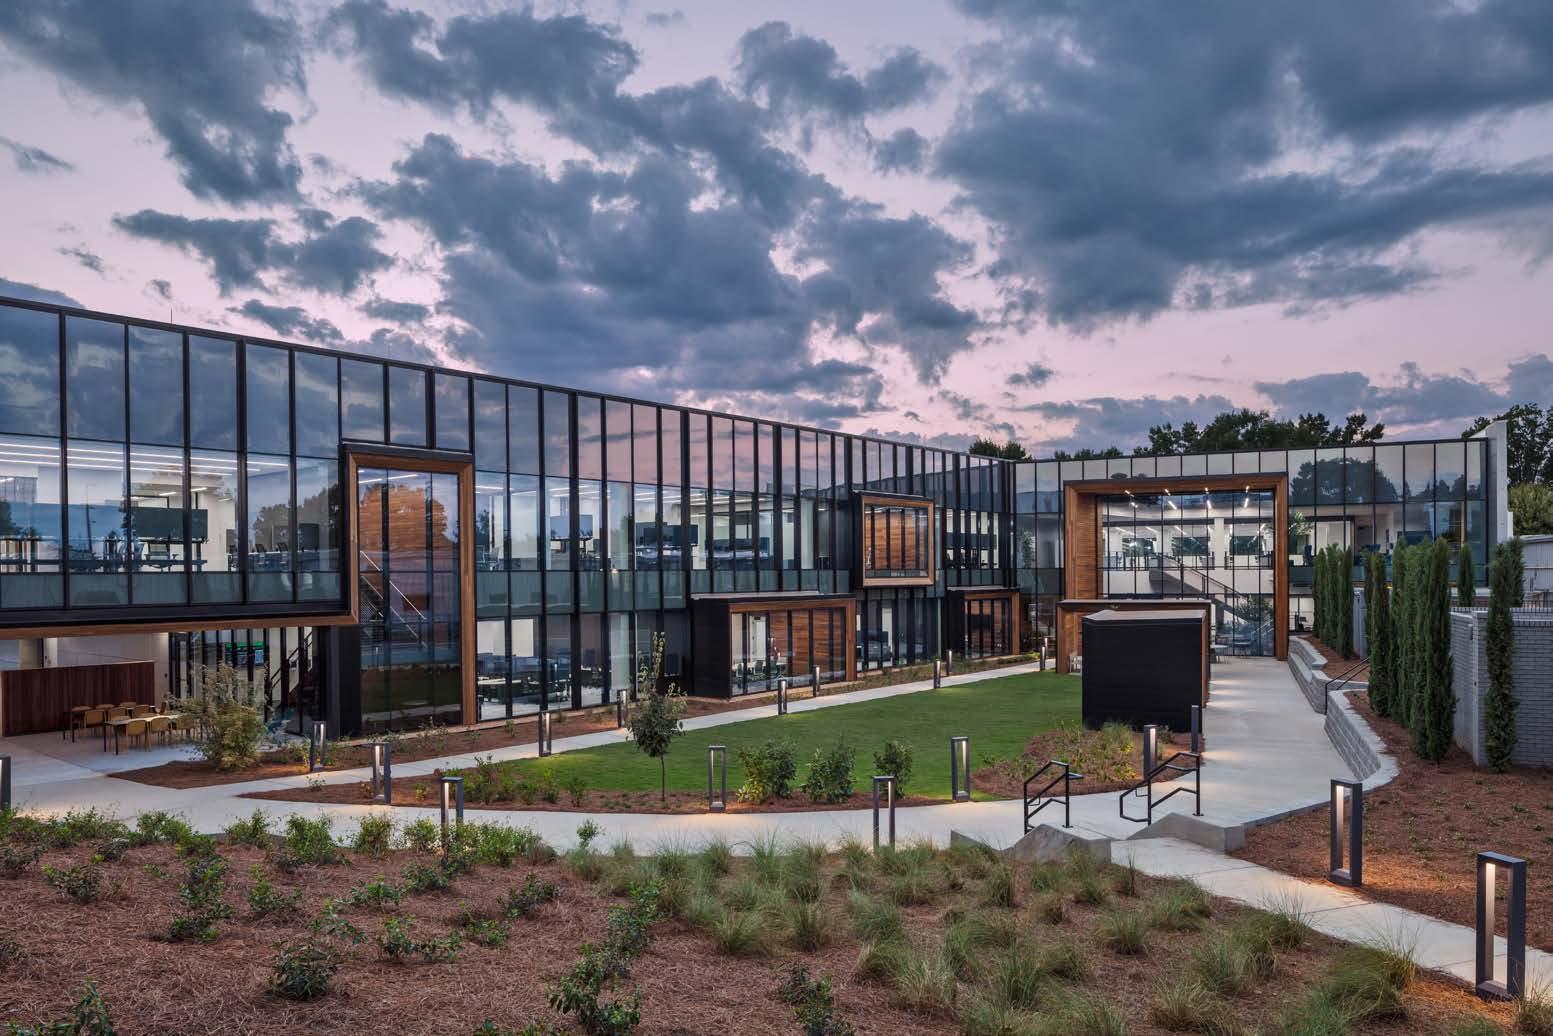
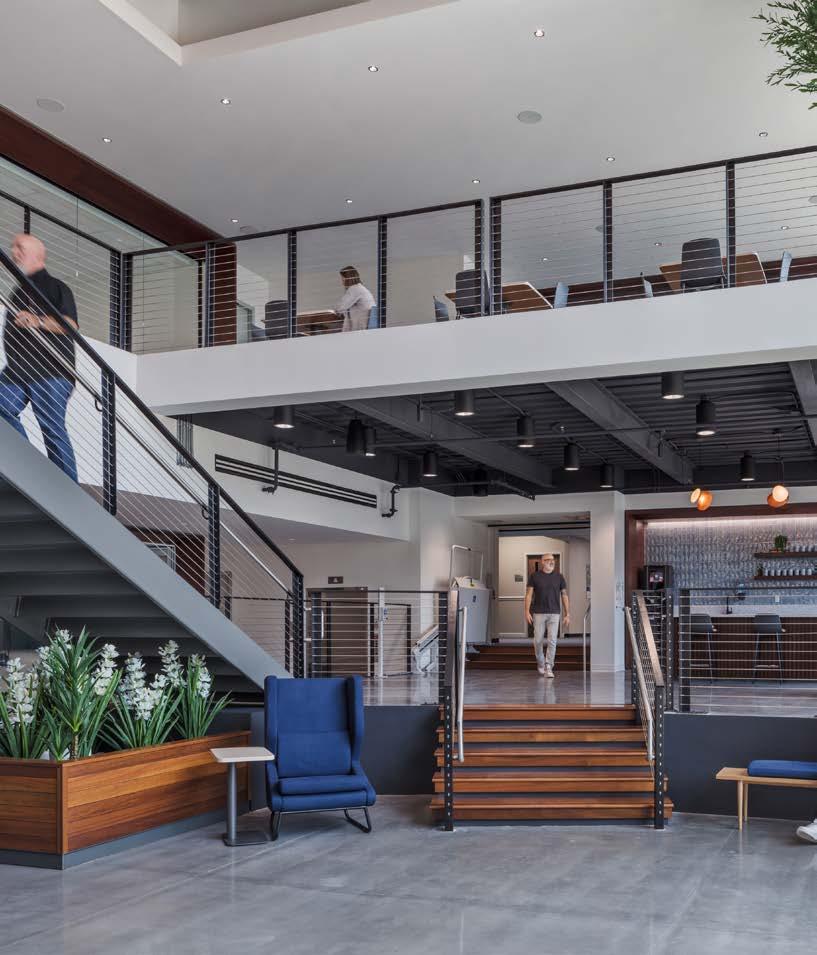
This state-of-the-art R&D hub unites research and administrative teams under one roof, fostering collaboration and accelerating breakthroughs in animal health. CRB managed every phase—from feasibility and design to construction—creating a space that inspires innovation while prioritizing sustainability and occupant well-being.
Sustainability:
Energy-efficient systems and materials aligned with LEED Silver standards.
Open, activity-based workspaces: Flexible seating and collaborative zones encourage knowledge sharing.
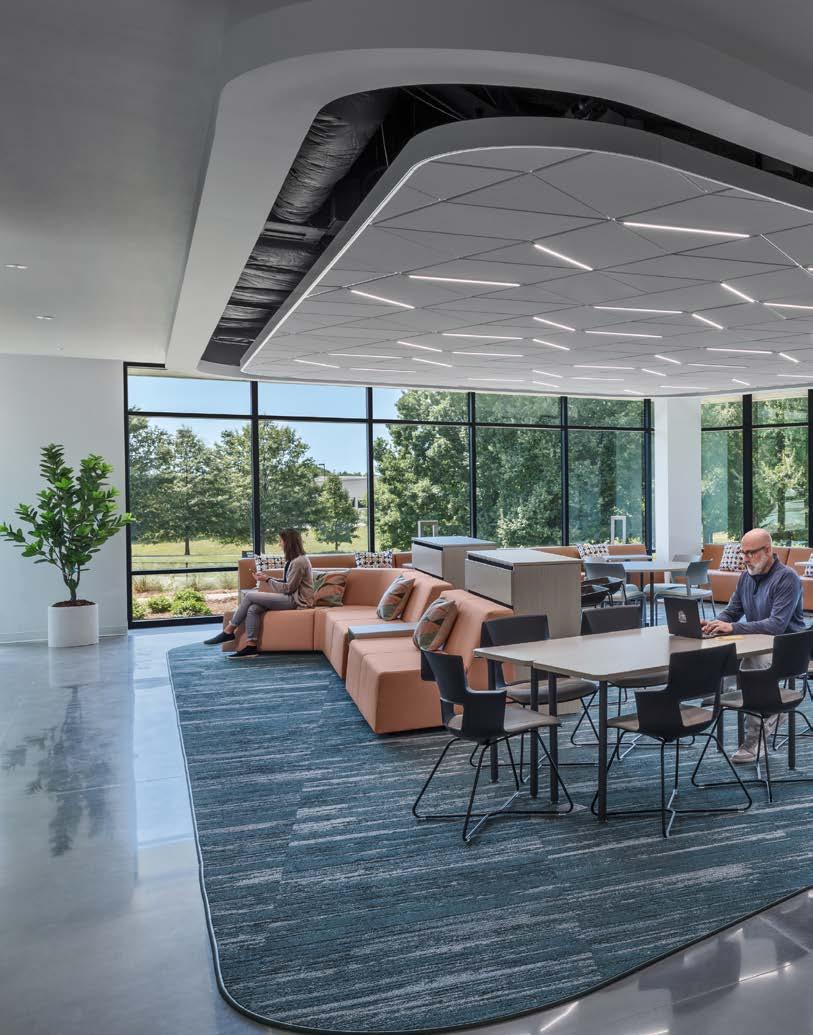
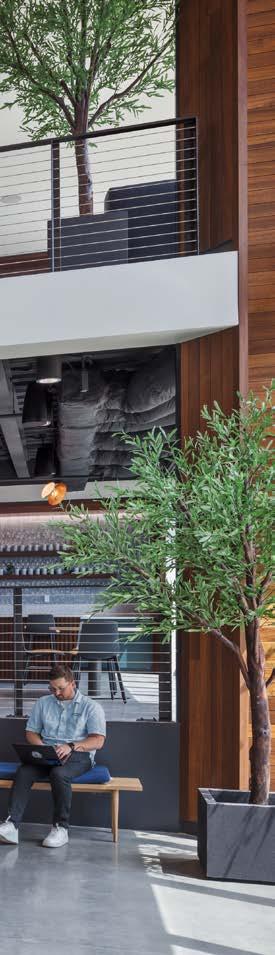
Integrated labs: Multiple BSL-2 labs support advanced research capabilities.
Natural light and biophilic design: Expansive windows and natural finishes create a healthy, inspiring environment.
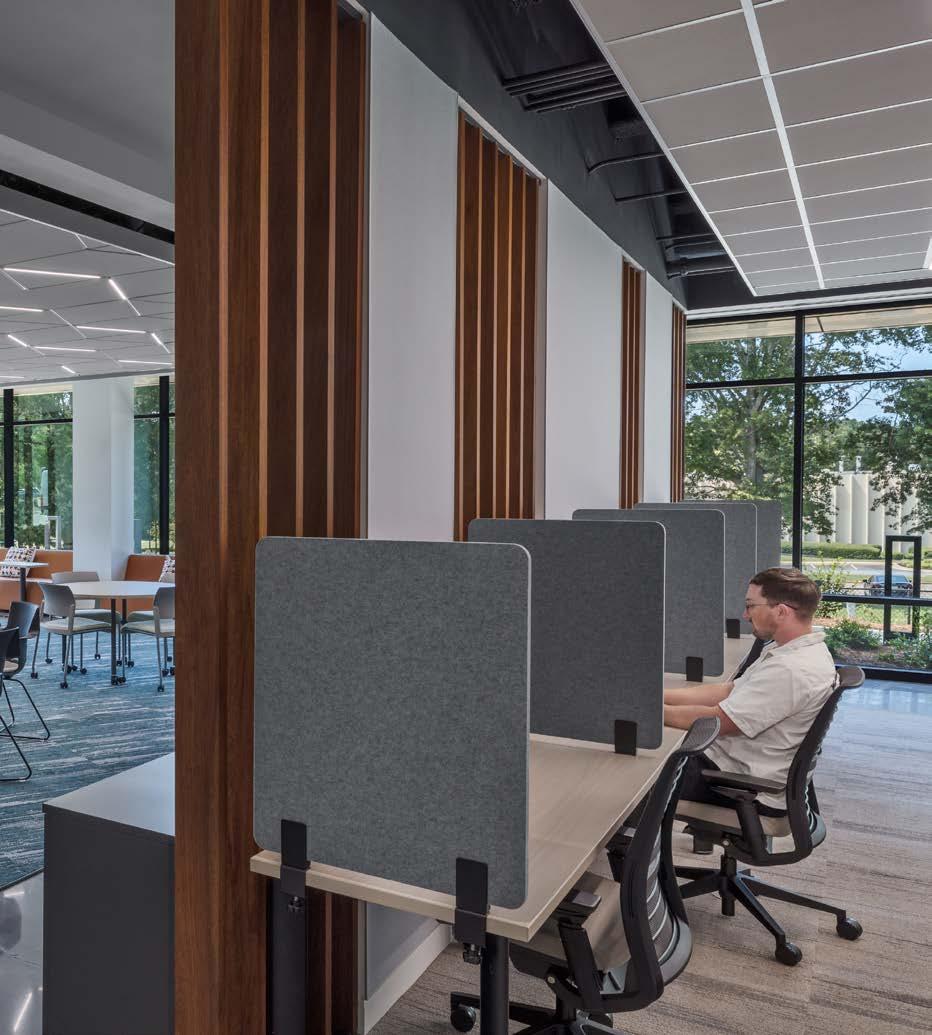
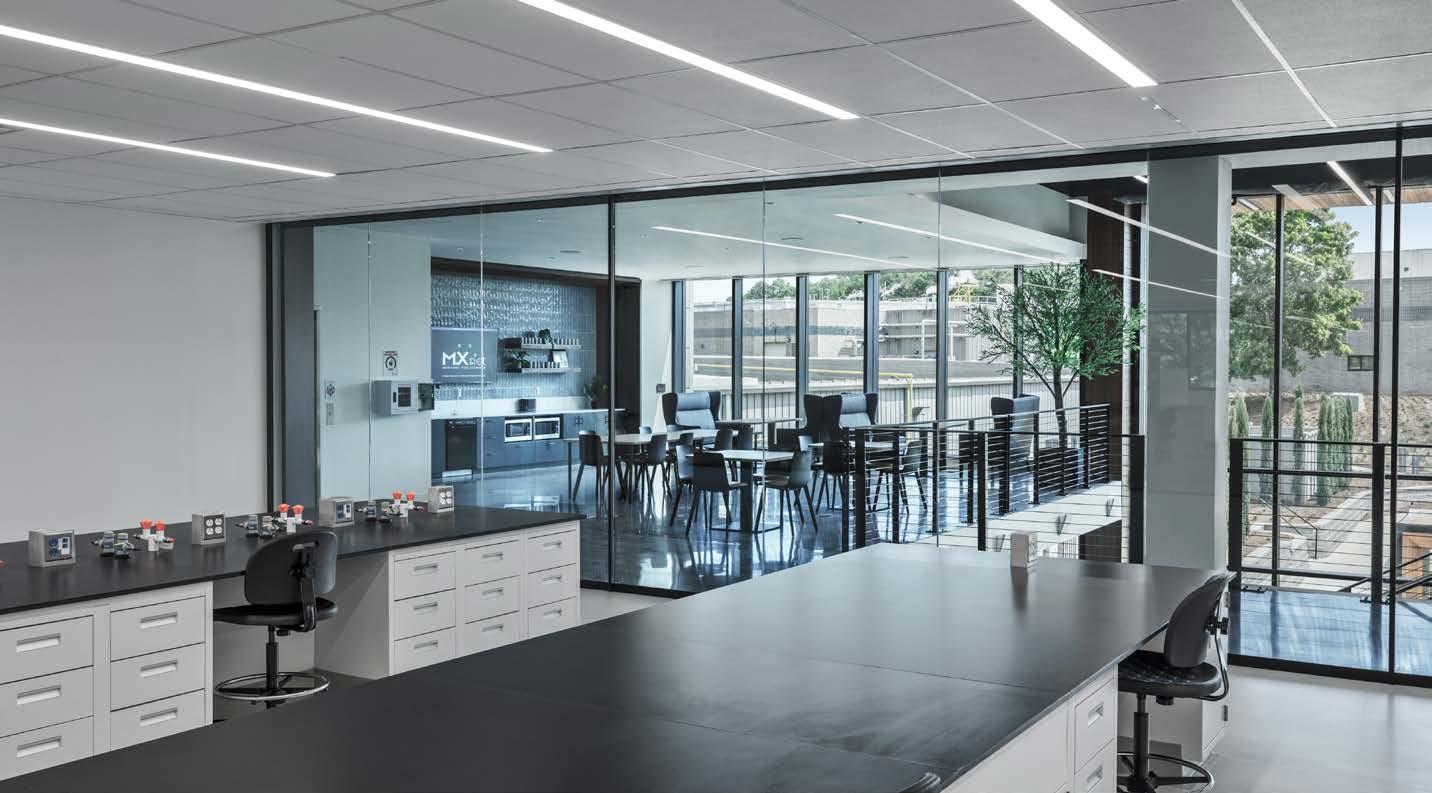
Outdoor courtyard: Outdoor courtyard for meetings and team gatherings connecting the new building to the campus.
Design development
Project delivery
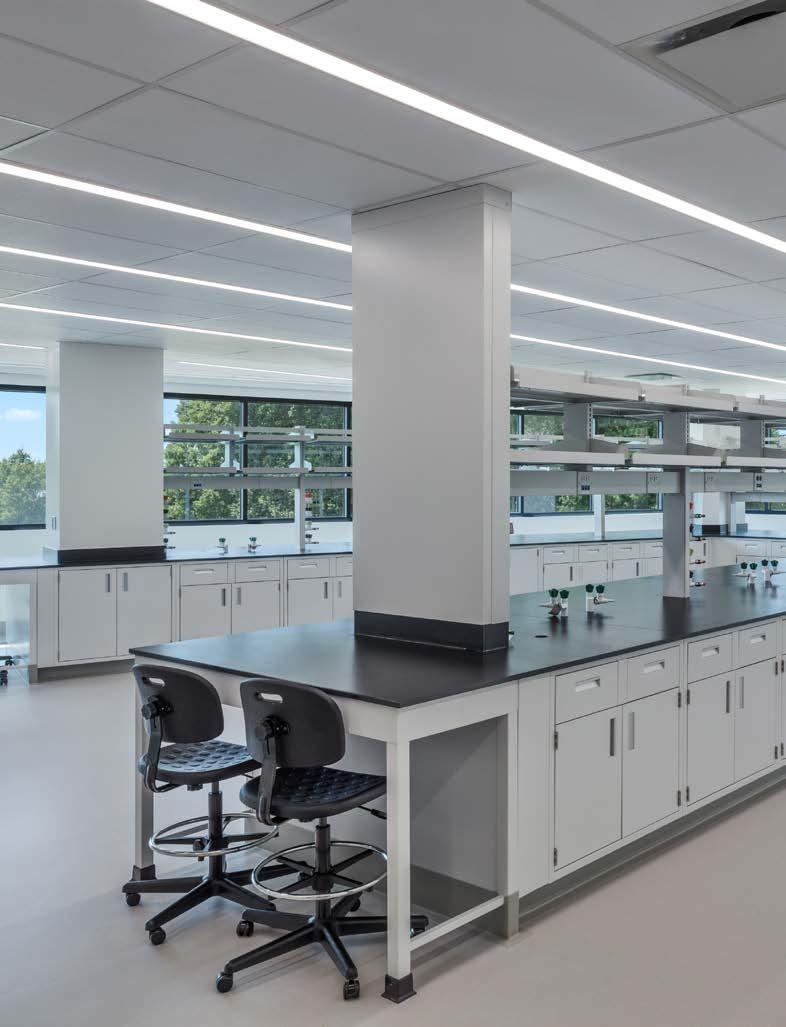
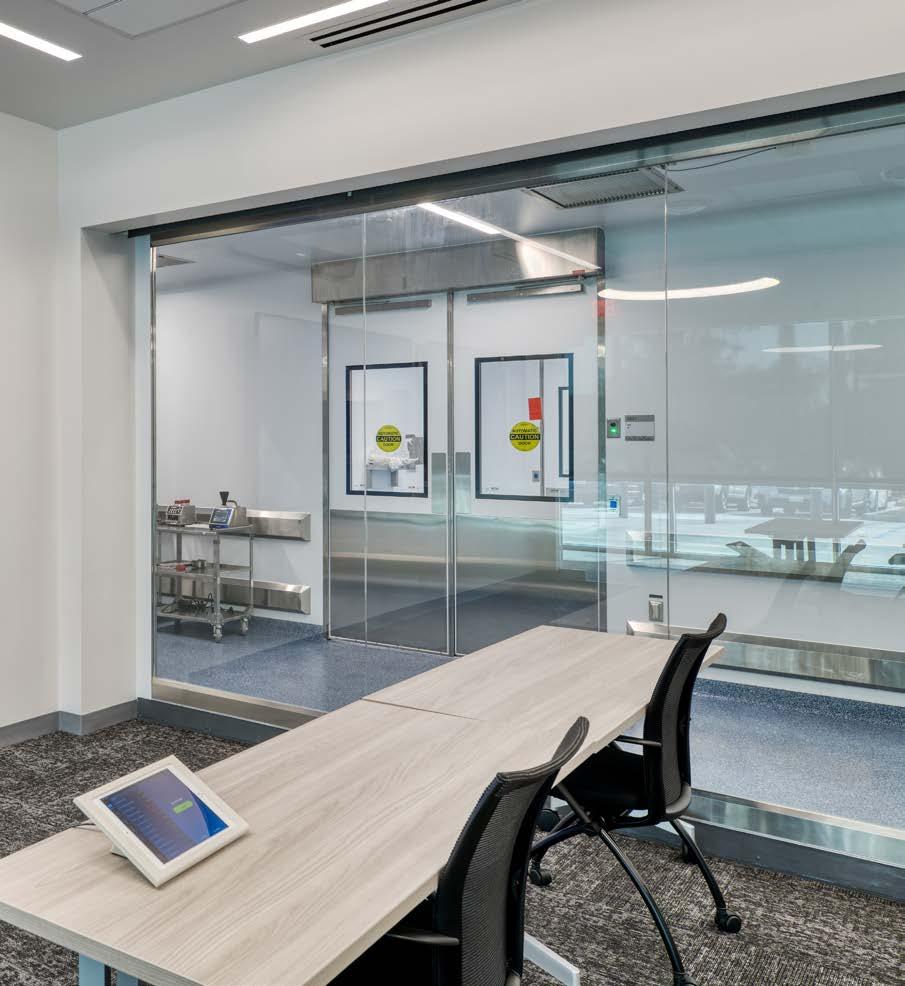
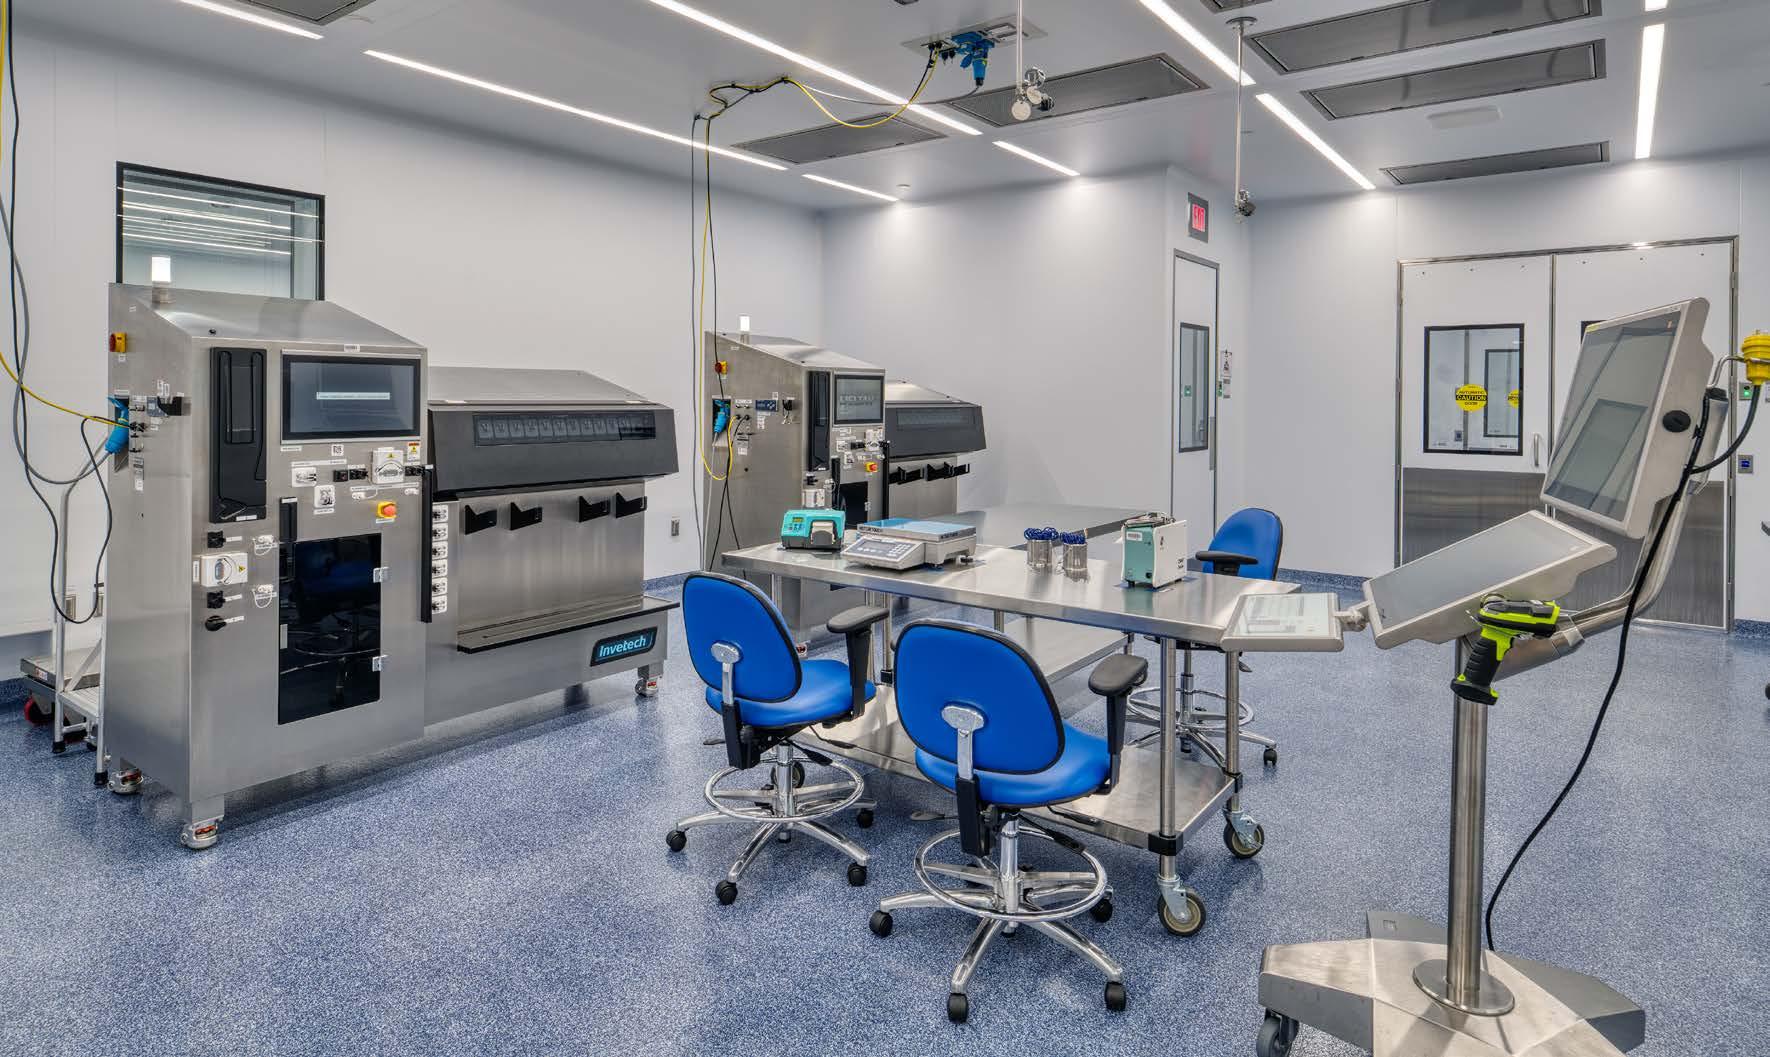
Kite, a Gilead company, advances cancer immunotherapy through CAR-T cell therapies supported by its 67,000 sq ft MVP01 facility for flexible, scalable viral vector manufacturing. By internalizing vector production, the facility strengthens supply chain resilience, accelerates development timelines, and supports rapid innovation critical to patient specific therapies. Co-locating biological development and manufacturing enables seamless collaboration, consistent quality standards, and efficient technology transfer, while a robust safety culture, ergonomic design, and biosafety planning ensure a secure workplace. With LEED Gold–certified sustainability features, the facility sets a new benchmark for efficient, responsible delivery of life changing treatments.
Front-end planning
Design development Lifecycle
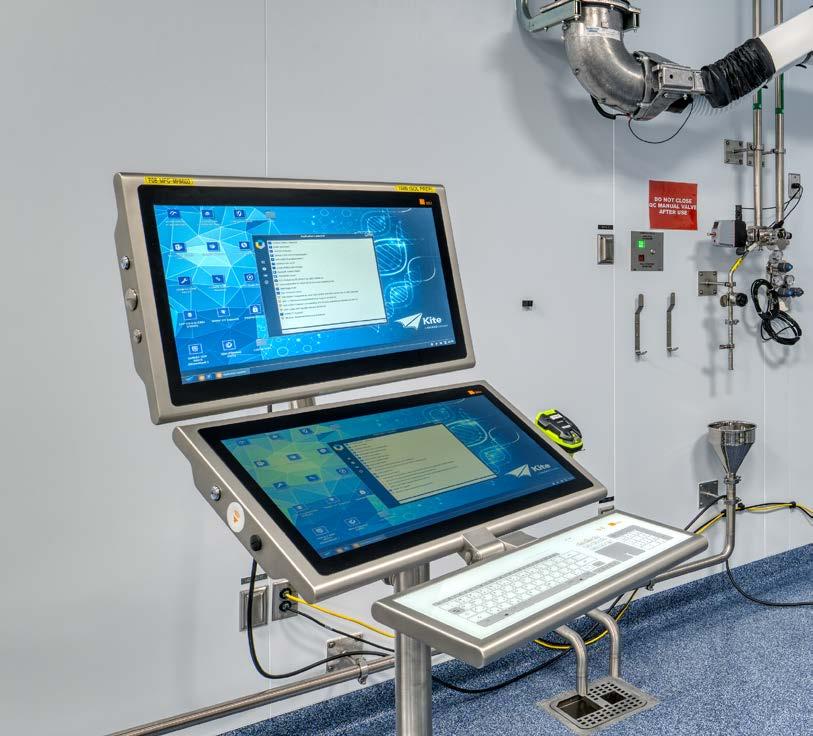
“At Kite, we regularly do things for the first time ever and this facility is no exception. We’re leaning into complete control of the end-to-end process, including gene editing. These developments are radically changing the types of medicines we can make for people and the ways we make them.”
Will Junker, Head of Vector Manufacturing Quality, Kite
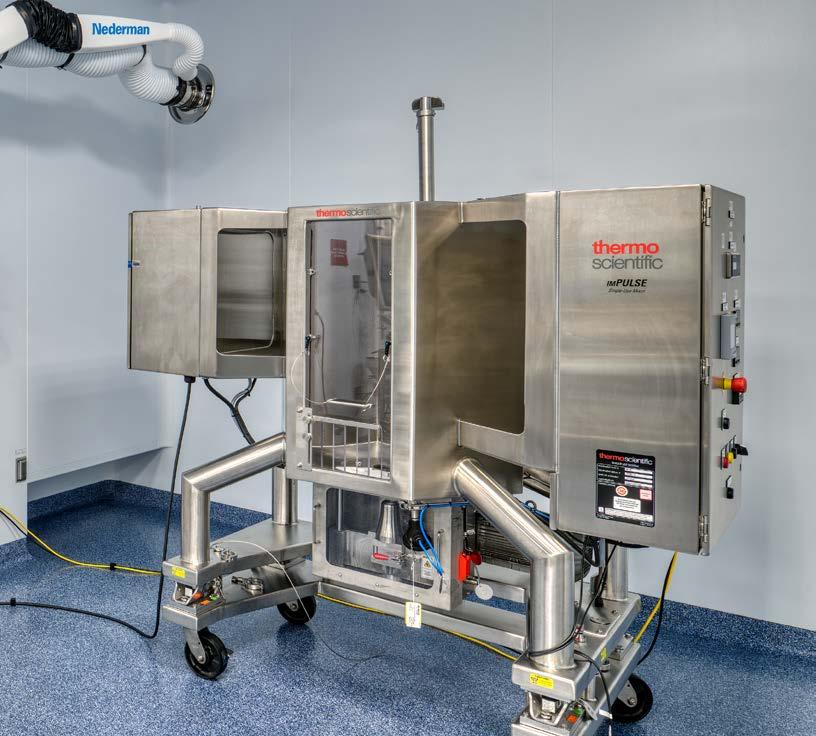
Concurrent multi-product manufacturing: Two dedicated production trains enable simultaneous production of multiple viral vectors.
Modular, flexible design: Facility can double capacity and adapt to future needs.
Advanced segregation: Segregated suites, HVAC, and unidirectional flow minimize cross-contamination.
Pharma 4.0 automation: Minimizes cross-contamination and enables paperless, real-time operations.
CRB people are in constant pursuit of learning, sharing and providing world-class technical excellence. While we are innovative and forward-thinking, we believe our first and foremost responsibility is to provide the right solution that meets our clients’ technical and design needs.
For two decades, CRB’s thought leaders have been involved in the development of pharmaceutical industry standards, including authoring and co-authoring 20+ ISPE Guides. Our Senior Fellows and Fellows lead the development and implementation of cutting-edge technologies and innovations and champion growth programs within the company.
Our subject matter experts are sought-after speakers and authors, providing insights on the technical challenges affecting advanced technology clients today and in the future. We are proud to contribute to the best practices that deliver cost effective, safe and successful solutions for our clients and the industry.
By seeking out client insights and combining it with our expertise, we facilitate knowledge sharing within the communities and industries we serve.
Backed by insights from 400 global R&D and manufacturing leaders, the Horizons: Life Sciences report reveals how the industry is building resilience, expanding pipelines, and empowering a motivated workforce to push innovation forward despite trade turbulence and regulatory flux.
Download the report
This report is designed to understand how food and beverage manufacturers are prioritizing capital investment, production growth, and food safety improvements in the year ahead. Early industry signals suggest that many companies are planning to increase production capacity, yet food safety remains one of the most persistent and complex challenges influencing these investments.
Download the report
Our Horizons: Market Conditions report is a snapshot of the construction economy that addresses the challenges of capital project planning for life sciences and food and beverage industries. It covers supply chain, escalation, labor and more.
Download the report
Whether you are shaping the future of pharmaceuticals, consumables or technologies—CRB is here to design and build the facilities that will help achieve your goals.
Let’s write our next chapter by creating powerful solutions together.
Built with purpose. Delivered with confidence. Contact us