the Analyst The Voice of the Water Treatment Industry
Volume 27 Number 1
1300 Piccard Drive, Suite LL 14 • Rockville, MD 20850
Winter 2020
Stabilization of the Magnetite Layer in Steam Boilers With Tannins Can Induction Time Methods Aid in Evaluation of Calcium Carbonate and Calcium Phosphate Scale Inhibitors? How Operating Risks Should Be Managed in Industrial RO Systems Part 5: An Overview of IX Resins for Water Treatment Can a Non-Chemical UV Dechlorination System Improve RO System Performance?
Volume 27 Number 1 Winter 2020
Published by
WE PUT THE PIECES TOGETHER.
Designed to complete your water treatment system.
MicroVision EX makes life simpler for water treaters. Our advanced controller is easier to install, program and operate because of proven MicroVision software that utilizes an intuitive user interface. Accurate measurement is achieved by our toroidal probe, which is factory-calibrated and maintenance-free. And PULSAlink cloud-based communication delivers convenience and the highest security. MicroVision EX controllers, maintain process control, reduce costs and limit downtime, freeing up more time for water treaters to serve their customers. Only with MicroVision EX from Pulsafeeder. MicroVision EX Offers • Toroidal Conductivity Sensor • Choice of additional sensors: pH, ORP, PTSA, and Corrosion • Customization: Relays, water meters, inputs, reports and graphing • PULSAlink Communications: Web and iOS/Android App • Plus much more
Models designed or High Pressure applications up to 300 psi.
Corrosion Sensor models available with choice of mild steel or copper metal tips.
The MicroVision EX can be ordered with Modem Millie, offering you a complete system right out of the box.
Don’t bother with an incomplete controller. Install the MicroVision EX from Pulsafeeder.
Install Wizard.
Using the Install Wizard on all MicroVision EX controllers makes configuring installation files error proof, customizable and fast.
Modbus BMS integration.
MicroVision Ex controllers equipped with an Ethernet interface can connect to a SCADA system via Modbus TCP communication protocol.
Flow Meter Integration.
Excellent precision and versatility, integrates through Hall Effect water meter inputs for calibrated results. Charting scaled with time-corroborate with probe readings and relay states + total chemical dosed.
To learn more, contact your Pulsafeeder sales rep at pulsatron.com today!
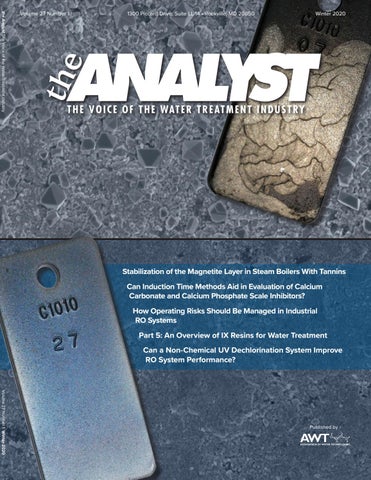
Cover Top: Photomicrograph of an untreated corrosion coupon, which is inserted within the image. Bottom: Photomicrograph showing a corrosion coupon (inserted into the image) treated with tannins. Photos courtesy TGWT Clean Technologies/Louis Godbout.
Winter 2020
Volume 27
Number 1
8 Stabilization of the Magnetite Layer in Steam Boilers With Tannins
Louis Godbout (TGWT, Inc.); Axel Gambou-Bosca, Ph.D. (Centre de métallurgie du Québec); and Christian Fowelin, Ph.D. (Korn GmbH)
After having been the treatment of choice for boiler corrosion and scale control for more than a century, the use of tannins decreased in the 20th century in favor of cheaper, but often underperforming synthetic products. Resurgence in their use is now underway because of the energy and water savings they allow and other environmental benefits of green chemistry.
28 Can Induction Time Methods Aid in Evaluation of Calcium Carbonate and Calcium Phosphate Scale Inhibitors?
Bill Glover, Ph.D., and Kaylie L. Young, Ph.D. (Dow Chemical), and Robert J. Ferguson (French Creek Software)
Scale-inhibitor testing in the laboratory is the first step in providing reliable information for comparing the efficacy of scale inhibitors of different chemistries and between different manufacturers. Unfortunately, the laboratory tests and the reporting of results are not standardized across the industry, so each scale-inhibitor manufacturer is free to choose arbitrary conditions under which they conduct their testing. Although not maliciously misleading, the testing may present a limited view of the product performance.
40 How Operating Risks Should Be Managed in Industrial RO Systems
Loraine A. Huchler, P.E., MarTech Systems Inc.
The objective of this article is to provide options for avoiding or mitigating common risks of operating reverse osmosis (RO) systems installed in industrial facilities. The most common risks in industrial facilities include inadequate pretreatment, poor idling strategies, and improper or insufficient cleaning protocols. This article defines best practices for the design and operation of RO units and includes several case histories that describe the impact of the most common design and operating risks for RO units in industrial facilities.
52 Part 5: An Overview of IX Resins for Water Treatment
Peter Meyers, ResinTech Inc.
This is Part 5 of a series of articles that have covered various aspects of how ion exchange (IX) resins are used. This part brings together the information shared in Parts 1 through 4 and covers general resin use, including what resins are, safety aspects related to resins, materials compatible with resin, contamination of resin, and documentation associated with their use.
4
Calendar of Events
5
President’s Message
6
Message From the President-Elect
72 Membership Benefits 73 Association News 74 Industry Notes 77 CWT Spotlight 78 Making a Splash 79 Capital Eyes 82 Financial Matters 83 Business Notes 85 T.U.T.O.R. 90 Advertising Index
64 Can a Non-Chemical UV Dechlorination System Improve RO System Performance?
R. Aaron Nickles, Southern Company—Plant Bowen
Georgia Power’s Plant Bowen, a 3,160-megawatt coal-fired power station located in Cartersville, Georgia, has faced frequent reverse osmosis (RO) membrane and cartridge filter maintenance and replacement issues in recent years. The RO and cartridge filter system problems were caused by biological fouling and oxidation, despite the power station’s use of a sodium metabisulfite (SMBS) dechlorination process. As a result, Plant Bowen on a trial basis tested three non-chemical ultraviolet (UV) dechlorination treatment systems in March 2014, with the aim of improving the quality of the RO feedwater. At the conclusion of the evaluation period, UV dechlorination technology had effectively removed free and total chlorine from boiler feedwater to undetectable levels from inlet free and total chlorine levels above 1 part per million (1).
3
the Analyst Volume 27 Number 1
1300 Piccard Drive, Suite LL 14 Rockville, MD 20850 (301) 740-1421 • (301) 990-9771 (fax) www.awt.org
2020 AWT Board of Directors President
Thomas Branvold, CWT
Calendar of Events
Association Events 2020 Technical Training (East)
Secretary
March 18–21, 2020 Marriott Cleveland Cleveland, Ohio
Treasurer
2020 Annual Convention & Exposition
President-Elect
Michael Bourgeois, CWT Matt Jensen, CWT
September 30–October 3, 2020 Louisville Convention Center and Omni Hotel Louisville, Kentucky
Stephen C. Hallier, CWT
Immediate Past President
David Wagenfuhr
Directors
Noah Baskin Mark Coldren, CWT Stephanie Keck, CWT Andy Kruck, CWT
2021 Annual Convention & Exposition
Ex-Officio Supplier Representative
Garrett S. Garcia
Past Presidents
Jack Altschuler John Baum, CWT R. Trace Blackmore, CWT, LEED AP D.C. “Chuck” Brandvold, CWT Brent W. Chettle, CWT Dennis Clayton Bernadette Combs, CWT, LEED AP Matt Copthorne, CWT James R. Datesh John E. Davies, CWT Jay Farmerie, CWT Gary Glenna Charles D. Hamrick Jr., CWT Joseph M. Hannigan Jr., CWT Mark R. Juhl
Brian Jutzi, CWT Bruce T. Ketrick Jr., CWT Bruce T. Ketrick Sr., CWT Ron Knestaut Robert D. Lee, CWT Mark T. Lewis, CWT Steven MacCarthy, CWT Anthony J. McNamara, CWT James Mulloy Alfred Nickels Scott W. Olson, CWT William E. Pearson II, CWT William C. Smith Marc Vermeulen, CWT David Wagenfuhr Casey Walton, B.Ch.E, CWT Larry A. Webb
Staff
Executive Director
Heidi J. Zimmerman, CAE
Deputy Executive Director
Sara L. Wood, MBA, CAE
Senior Member Services Manager
Angela Pike
Vice President, Meetings
Grace L. Jan, CMP, CAE
Meetings Manager
Ivy Caro, GCMP
Meetings Manager
Morgan Prior
Exhibits and Sponsorship Manager
Barbara Bienkowski, CMP
Senior Marketing Director
Julie Hill
Marketing Director
Jennifer Olivares
Technical Writer/Copy Editor Lynne Agoston
Accountant
Dawn Rosenfeld
The Analyst Staff
Publisher, Heidi J. Zimmerman, CAE Managing Editor, Lynne Agoston Production Manager, Maryia Alenchyk Technical Editor Michael Henley (303) 745-3890 mdhenleywater@gmail.com
Advertising Sales
Heather Prichard advertising@awt.org
The Analyst is published quarterly as the official publication of the Association of Water Technologies. Copyright 2020 by the Association of Water Technologies. Materials may not be reproduced without written permission. Contents of the articles are the sole opinions of the author and do not necessarily express the policies and opinions of the publisher, editor or AWT. Authors are responsible for ensuring that the articles are properly released for classification and proprietary information. All advertising will be subject to publisher’s approval, and advertisers will agree to indemnify and relieve publisher of loss or claims resulting from advertising contents. Editorial material in the Analyst may be reproduced in whole or part with prior written permission. Request permission by writing to: Editor, the Analyst, 1300 Piccard Drive, Suite LL 14, Rockville, MD 20850, USA. Annual subscription rate is $100 per year in the U.S. (4 issues). Please add $25 for Canada and Mexico. International subscriptions are $200 in U.S. funds.
September 22–25, 2021 Providence Convention Center and Omni Hotel Providence, Rhode Island
2022 Annual Convention & Exposition September 21–24, 2022 Vancouver Convention Centre Vancouver, Canada
2023 Annual Convention & Exposition
October 4–7, 2023 Grand Rapids Convention Center and Amway Grand Hotel Grand Rapids, Michigan
Also, please note that the following AWT committees meet on a monthly basis. All times shown are Eastern Time. To become active in one of these committees, please contact us at (301) 740-1421. Second Tuesday of each month, 11:00 am – Legislative/Regulatory Committee Second Tuesday of each month, 2:30 pm – Convention Committee Second Wednesday of each month, 11:00 am – Business Resources Committee Second Friday of each month, 10:00 am – Special Projects Subcommittee Second Friday of each month, 11:00 am – Cooling Subcommittee Second Friday of each month, 2:00 pm – Pretreatment Subcommittee Third Monday of each month, 9:00 am – Certification Committee Third Monday of each month, 3:30 pm – Young Professionals Task Force Third Tuesday of each month, 3:00 pm – Education Committee Third Friday of each month, 9:00 am – Boiler Subcommittee Third Friday of each month, 10:00 am – Technical Committee Quarterly (call for meeting dates), 10:00 am – Wastewater Subcommittee
Other Industry Events
NACE, Corrosion Conference & Expo, March 15–19, 2020, Houston, Texas ACS, Spring National Meeting & Expo, March 22–26, 2020, Philadelphia, Pennsylvania AWWA, Annual Conference & Expo, June 14–17, 2020, Orlando, Florida BOMA, Annual Meeting, June 27–30, 2020, Philadelphia, Pennsylvania ASHRAE, Annual Meeting, June 27–July 1, 2020, Austin, Texas ACS, Fall National Meeting & Expo, August 23–27, 2020, San Francisco, California NACE, Corrosion Technology Week, September 13–17, 2020, Houston Texas WEFTEC, Annual Technical Exhibition and Conference, October 3–7, 2020, New Orleans, Louisiana
4
the Analyst Volume 27 Number 1
President’s Message
By Tom Brandvold, CWT
fantastic opportunity to spend time talking about the business side of water treatment—about good customer service, cybersecurity, HR, innovation, and contracts. I was able to learn from others about the smart and creative ways different companies handle things, such as building a great team and improving customer loyalty. It was a really great meeting, and I came away with lots of actionable takeaways.
We recently had an account where Legionella developed. For years we had been recommending that this company adopt a water management plan. It hadn’t taken that advice, so when Legionella was detected, there was a four-alarm fire drill—over the holidays, no less—to address it. And while the outbreak had nothing to do with our role at the facility, as the water treater, we were, of course, pulled in. This meant having many staff at this facility for days at a time, throwing off our entire service schedule. As a relatively small company, this has a big impact on the entire system. And I have a feeling I’m not alone in this experience, as I suspect this is happening— and will continue to happen—more and more often.
If you’re a business owner, I hope you think about this and other trainings offered by AWT. The Technical Training Seminars are a great way to offer educational opportunities to your employees. And the Annual Convention is your go-to place to visit all of your vendors under one roof and learn about the latest innovations in our industry.
So, how do you provide the great service your company is known for, put out the ever-rising fires, and continue to grow and expand your business? My solution is to take time working on the business of running the business.
I look forward to seeing you at an upcoming AWT event this year! Thank you for the opportunity to serve. I can be reached at carmac@premierwater.com. Tom Brandvold President
I recently had the great pleasure of attending the AWT Business Owners Meeting. I am always so impressed by all of my peers in the industry. The meeting was a
5
the Analyst Volume 27 Number 1
Message From the President-Elect
cart paths bring these 18 holes together, connecting tee boxes for every golfer’s skill level to the course’s Zoysia grass fairways. Multiple lakes and strategically placed bunkers add to the beauty of the slightly undulated greens. Covered Bridge is a demanding yet fair test for every golfer.
Work is progressing on the 2020 Annual Convention & Exposition, which will take place September 30–October 3, in Louisville, Kentucky.
Educational Program
Annual Reception and Awards Dinner
We are currently putting together the program for the 2020 Convention, and we have some great abstracts from which to choose. I’m confident we will have a solid program with quality sessions. Our hope is to continue to have more panel discussions and educational workshops, which attendees told us they enjoy.
I’m very happy to report that the Annual Reception and Awards Dinner will be held at Churchill Downs, home of the Kentucky Derby. Horse racing in Kentucky dates back to 1789, when the first race course was constructed in Lexington. Almost 100 years later, in 1875, Churchill Downs officially opened its gates in Louisville and began its tradition as the longest continually running sporting event in America.
We have also received great feedback on the Commercial Corner sessions, so we will be adding more of these to the program. Be sure to mark your calendar for the meeting!
The details of the Annual Reception and Awards Dinner are being worked out, but in addition to the awards segment of the evening, there will be entertainment and tours. It will be a memorable event!
Golf
Our annual golf tournament will be held at Fuzzy Zoeller’s Covered Bridge Golf Club. Covered Bridge is a Fuzzy Zoeller/Clyde-Johnston-design 18-hole golf course carved through the gorgeous landscape of southern Indiana. Each hole of this par 72 layout offers a new and exciting challenge from tee to green. Paved
As we continue to plan the 2020 Convention, I welcome your feedback. I can be reached at mbourgeois@chemcoprod.com. Thank you for the opportunity to serve.
West Coast: February 26–29, 2020
Trainings available include:
Hyatt Regency Lake Washington | Seattle, Washington
• Sales
East Coast: March 18–21, 2020
• RO/Ultrafiltration •
Fundaments and Applications
•
Water Treatment
•
Wastewater (West Coast Only )
By Michael Bourgeois, CWT
Cleveland Marriott Downtown | Cleveland, Ohio
Sign up now at https://www.awt.org/tt2020/
6
the Analyst Volume 27 Number 1
Save the Date
2020 ANNUAL CONVENTION & EXPOSITION S E PT E M B E R 3 0 – O C TOB ER 3 , 2 020
LOUISVILLE
KENTUCKY Kentu c
ky Intern
enter C n o i t n ational Conve
Mark your calendar for the 2020 Annual Convention & Exposition! Kentucky International Convention Center and Omni Louisville Hotel Louisville, Kentucky Visit www.awt.org for more details.
b
Abstract
After having been the treatment of choice for boiler corrosion and scale control for more than a century, the use of tannins decreased in the 20th century in favor of cheaper, but often underperforming synthetic products. Resurgence in their use is now underway because of the energy and water savings they allow and other environmental benefits of green chemistry. Until recently, the empirically proven benefits of tannins were not understood scientifically. This is largely because their complex chemistry and structures have only been tackled in the past decade. The physico-chemical reactions occurring in the boilers are also finally becoming clearer. It was recently demonstrated that tannins adsorb on various metal surfaces. We have now further advanced our understanding of how this adsorption affects the development of the passivation layer of steel in boiler conditions. At high pH, temperature, and pressure, steel coupons rapidly develop a strikingly different appearance in the presence of tannins. Typically, the surface is visibly smoother and more adherent, with noticeably less spalling of magnetite than in control samples. We have studied the microstructure of these passivation layers using scanning electron microscopy coupled with energy dispersive spectroscopy (SEM/ EDS) as well as grazing incidence X-ray diffraction (GI-XRD). Their corrosion behavior was studied by potentiodynamic polarization and electrochemical impedance spectroscopy (EIS). The differences in thickness, porosity, adherence, crystal composition, and structure are in line with improved performances. These characteristics also explain why the use of tannins rapidly brings down to a minimum the evolution of hydrogen in boiler steam: a denser and less porous passivation layer becomes stable as it limits the Schikorr reaction at the underlying metal surfaces.
Stabilization of the Magnetite Layer in Steam Boilers With Tannins Louis Godbout (TGWT, Inc.); Axel GambouBosca, Ph.D. (Centre de métallurgie du Québec); and Christian Fowelin, Ph.D. (Korn GmbH)
How Magnetite Films Form
The study of films with reduced reactivity that protect an underlying metal from corrosion started in the 18th century (1), and then sparked the interest of Michael Faraday in the 1830s. The term “passivity” was coined by Faraday’s friend and collaborator, Christian Schönbein, in 1836. Together they quickly
8
the Analyst Volume 27 Number 1
understood that passivation involved the creation of a protective layer of metal oxide on the surface of the steel (2). This “bluing” or “blackening” of steel could be obtained either by heating, or by chemical or electrochemical treatment. It was and remains important in manufacturing and can be seen in many objects used in everyday life, such as screws, bolts, springs, and all sorts of tools.
The reaction (Equation 1) that produces magnetite was first described by Schikorr in 1933 (7): 3 Fe + 4 H 2O Fe3O4 + 4 H 2
Eq. 1
(N.B. This equation shows the reaction of iron and water to produce magnetite, but in fact Schikorr only described the transformation of iron hydroxide to magnetite: 3 Fe(OH)2 --- [150 °C] Fe3O4 + 2 H 2O + H 2)
Passivation remained a subject of great interest for many chemists through the 19th century. Great strides were made in the 20th century, especially with the development of electrochemical instrumentation (3). To this day, scientists have used the newest techniques to investigate the structure and formation of oxides and hydroxides that form on iron or steel. These will vary according to the conditions under which they form, but it is magnetite (Fe3O4) or, more precisely FeIIFeIII2O4 (i.e., ferrousferric oxide) that coats the surfaces of well-operated steel boilers and passivates them.
However, the simplicity of this overall reaction hides many other reactions and mechanisms that are vastly more complex but also more revealing of exactly how magnetite forms under different conditions of pH, temperature, pressure, and ionic conditions. Here is one series of proposed steps (Reactions 1-6) that may explain why it is favored in the boiler (8, 9). 1. Fe0 ↔ Fe2+ + 2e- EO = 0.44 V 2. Fe2+ + 6 H 2O [Fe(H 2O)6]2+ 3. [Fe(H 2O)6]2+ ↔ Fe(OH)2 +2H+ + 4 H 2O 4. 2 FeII(OH)2 + 2 H2O 2 FeIII(OH)3 + H2 5. n FeIII(OH)3 [FeIIIO(OH)]n + n H 2O 6. 2 [FeIIIO(OH)] + FeII(OH)2 Fe3O4 + aq
Magnetite was one of the first substances whose crystalline structure was determined by X-ray diffraction by W.H. Bragg, the founder of crystallography himself, in 1915 (4) (Figure 1).
Reaction 1 Reaction 2 Reaction 3 Reaction 4 Reaction 5 Reaction 6
Figure 1: (Left) An X-ray diffraction pattern of a magnetite crystal growing epitaxially from a steel surface. (Right) the crystal structure of magnetite. The black spheres are Fe3+, the green spheres are Fe2+, and the red spheres are O2 −. As Bragg described it in 1915, “The divalent atom lies at the centre of a tetrahedron of oxygen atoms, and the trivalent at the centre of an octahedron” (4). (Note: Figure 1 images are from References 5 and 6.)
9
the Analyst Volume 27 Number 1
Stabilization of the Magnetite Layer in Steam Boilers With Tannins continued
At high pH, Reaction 3 would be favored, while Reaction 4 would proceed only at high temperatures such as are found in boilers. However, as we will see, things are much more complicated, as different reactions occur at different locations in the structures of passive layers as they grow. These can be single or multi-layered, more or less adhesive to the underlying steel, more or less porous, and hence, may confer different degrees of protection from corrosion. The magnetite formation rate will vary according to how these structures evolve. It would be desirable that this rate rapidly diminish to a minimum after a thin and dense layer of oxide is formed and prevents further oxidation, but this is rarely the case. In fact, under certain circumstances, oxidation of iron to magnetite can be an important source of metal loss if the layer is too porous and continuously spalls. Another source of worry with an undiminishing high rate of the Schikorr reaction is the production of hydrogen, which will readily diffuse through steel and embrittle it as it reacts with carbon to form methane. In fact, the monitoring of hydrogen in steam is recommended for high-pressure systems (10). Since the late 1950s, many researchers have attempted to understand and categorize the various morphologies of the magnetite layers. The pioneers were Bloom, Potter, Mann, Castle, Field, Friggen, Holmes, Marsh, and Moore, who produced magnetite passivation layers in autoclaves under controlled conditions (6, 11–21). They characterized them by microscopy and by measuring the rate at which the layer was produced, either by monitoring the evolution of hydrogen or by measuring the weight gained as magnetite formed on the surfaces. Two major morphologies were described and came to be known as “Bloom films,” which consist of a single thin
layer of large crystals, and “Potter-Mann films,” which consist of two thick layers—an underlying one of small compacted crystals and a top one of large and loosely bound crystals with well-defined spinel structure (see Figure 2). Much effort was invested in understanding how two such dissimilar structures could form under very similar conditions. In both experiments, steel samples with clean surfaces were oxidized at high temperature and pressure in caustic solutions. The only difference was that the Bloom films were produced in sealed steel capsules of relatively small volume, whereas the Potter-Mann films were produced in mild-steel pressure vessels of large volume, the interior of which was already covered with magnetite. For more than a decade, clever experiments were designed to understand how the different structures arose. It was determined that the Potter-Mann films formed because the fresh iron surfaces were in galvanic contact with magnetite previously formed on the insides of the autoclaves that acted as a cathode. More interestingly, it was determined that hydrogen concentration also affected the outcome. This is because hydrogen gas does not diffuse as easily through magnetite as it does through steel, whereas hydrogen ions do, leading to gradients and different reaction equilibria through the layer. This was to prove of great importance in understanding the mechanisms involved in the formation of multilayered films. These are more interesting, as they are the type seen in industrial systems, as opposed to “Bloom films,” which are seen only in controlled lab experiments. But how exactly they are formed was the subject of another four decades of research and is still ongoing.
Figure 2: (Left) A very thin, 5- to 10-micron (µm), single-layered “Bloom film” made of large crystals fused to the surface. (Right) A very thick, 40- to 50-µm, double-layered “Potter-Mann film” with a compact underlying layer of small crystals and a loose top layer of large, well-formed crystals. (Figure 2 is from Reference 19.)
10
the Analyst Volume 27 Number 1
Stabilization of the Magnetite Layer in Steam Boilers With Tannins continued
Understanding the reason for the small-grain morphology of the base layer came early. As iron is oxidized to magnetite, its volume increases about by a factor of 2.1 (the Pilling-Bedworth ratio); it is thus inevitable that stresses will be created that could fracture the crystals (22). The work of Moore and Jones (6), who followed the transformation of oriented crystals (emerging epitaxially from iron grains) into small randomly oriented crystals, demonstrated this convincingly. A thorough explanation of how the grains are reduced to their comminution limit by a cracking mechanism because of the compressive stresses was later given by Robertson and Manning (23). This cracking necessarily involves the creation of micro- or perhaps nano-pores, which are necessary to explain how a second layer develops. Understanding the reason for the larger, well-defined crystals found in the top layer may also seem obvious. It can only develop if there is iron transport from the oxide layer, as Castle and Mann believed (17), or from the underlying surface metal, as later models propose. The iron must remain in a soluble form as it moves through pores along grain boundaries in the base polycrystalline layer. Once it reaches the surface, it can be oxidized to magnetite that can grow unconstrained, from small
nuclei to very large crystals. The difficulty, however, was to elucidate why the pores remain unclogged, as one would expect that any iron in solution would precipitate to fill and block them. Two mechanisms to explain this were offered by Bignold, et al. (24), and by Bergé, et al. (25). The latter convincingly suggests that higher hydrogen levels at the metal-oxide surface and in the pores will reduce magnetite to a soluble hydroxide that can then migrate to the surface to be oxidized again and deposit on the larger magnetite crystals. Figure 3 presents cartoons of some of the models suggested over the years, showing what reactions occur and, more importantly, where. Refinements of these models that agree more closely with the measurements of reaction rates and the location of hydrogen evolution are still being proposed (9, 22). In parallel, even though the conditions are drastically different than in a boiler, studies of the structure of passivation films produced electrochemically (3, 26, 27) and spectroscopic studies that can detect the presence of various other iron oxides, such as the crystallographically close maghemite (28, 29) and hydroxides, may reveal more about what precisely happens in the formation of a magnetite film.
Figure 3: Various models proposed to explain the formation of the double-layered “Potter-Mann film” passivation layer. Clockwise from top left are Castle and Mann (17), Tomlinson (30), Cheng and Steward (31), and Shibata (32). The last two, as well as that of Bornak’s (33), are variants of Tomlinson’s model. That of Robertson (not presented here) is also noteworthy for its detailed unravelling of what reactions occur where in the structure, but it is not represented here graphically (22).
11
the Analyst Volume 27 Number 1
Stabilization of the Magnetite Layer in Steam Boilers With Tannins continued
“The most striking observations are the traces of blistering and spalling on the untreated coupons oxidized without tannins.” Unfortunately, many of the studies on the formation of magnetite films are limited to systems in which only sodium hydroxide (NaOH) or lithium hydroxide (LiOH) are present in pure water. A few have explored the effect of various metal chlorides, which seem to have a very negative effect, leading to the formation of multilayered, nonprotective passivation layers (16). Others have explored the effect of complexing agents and water treatment chemicals on the morphology and resistance of the passivation layer (34–39). In this study, we propose to evaluate the effect of tanninbased corrosion inhibitors on the magnetite layer, through experiments done in synthetic boiler water that is more realistic than the simple solutions heretofore used.
Materials and Methods
“Synthetic” boiler water was prepared using the following recipe (all reagent-grade chemicals were from Sigma-Aldrich):
Grazing incidence X-ray diffraction (GI-XRD) was done using a Bruker model D8 Advance instrument. The X-ray source was copper (Cu) (1.5418Å) with a 40 kilovolt (kV) voltage and a 40-milliamp (mA) current. The angle of incidence (2θ) was 3°. The primary source passed through a Göbel mirror (deflection of 0.876°) et axial Soller slits (2.5°) before hitting the sample. The secondary rays diffracted by the sample pass through Soller slits (0.2°), a nickel filter (0.02-millimeter (mm) thick), et axial Soller slits (2.5°) before hitting the detector. The diffractograms were acquired from 25° to 75°, in 0.02° increments and a 1-second integration time. Potentiodynamic polarization and electrochemical impedance spectroscopy (EIS) were performed in 3.5% NaCl solutions in a K0235 flat cell from London Scientific Limited using a Princeton Applied Research/ AMETEK VersaSTAT 4 potentiostat/galvanostat with a frequency response analyzer (FRA).
320 mg of anhydrous sodium sulfate (Na 2SO4)
Scanning electron microscopy (SEM) was performed using a JEOL JSM7600F instrument with a field-effect electron gun (FEG). Energy dispersive spectroscopy X-ray analysis (EDS) was performed with an Oxford Instrument detector and software.
500 mg of sodium chloride (NaCl)
Results and Discussion
4 milliliter (mL) of 1 M NaOH solution
General Visual Appearance of Coupons and Spalling of Magnetite Figure 4 shows unpolished coupons produced in four different experimental conditions. The polished coupons show similar features. The most striking observations are the traces of blistering and spalling on the untreated coupons oxidized without tannins. This is indicative of a weakly adherent magnetite layer. The blistering seems to have progressed through successive detachments, as shown by the “worming” path and shape of the traces. Similar zones were seen on both polished and unpolished coupons but give only a qualitative estimate of the quantity of loosely bound magnetite, more abundantly found at the bottom of the autoclave, as shown in Figure 5.
320 milligrams (mg) of anhydrous sodium carbonate (Na 2CO3)
The recipe was completed with reverse osmosis (RO) water to a volume of 1,000 mL. For each experiment, 50 mL of this solution was placed in a 100 mL Teflon® container designed to fit into a stainless-steel autoclave with a screw system to keep the contents sealed at high temperatures. After placing the autoclave in a glovebox, argon was used to displace any air and was bubbled through the solution for 30 minutes. Using a micropipette, 100 microliters (µL) of one of a tannin solution A was added. A C1010 steel coupon (either polished or unpolished) was placed inside, and the Teflon® cover secured. The metal cap of the autoclave was then screwed tightly before placing it in an oven at 180 °C for 96 hours. 12
the Analyst Volume 27 Number 1
Legionella
Laboratory
Indoor Air Quality
ONLYYOU CAN PREVENT LEGIONNAIRES' DISEASE
Environmental Safety Technologies Leading the way in Legionella testing since 1993...
• Legionella & Pathogen Testing • Detailed Legionella Laboratory Reports • Standard 7-10 Day and 96 Hour Rapid Turn-around • Emergency Outbreak Response The EST Team consists of a diverse group of professionals:
• Ph.D. Microbiologist • Certified Water Technologist • Certified Industrial Hygienist • Certified Indoor Air Quality Professional • Certified Healthcare Contractor • Certified Indoor Environmental Consultants • Laboratory Analysts • Environmental Specialist • Project Managers We pride ourselves on being competitively priced, offering personalized customer service that is flexible and responsive to our customers' needs.
Call us today to learn more about other waterborne pathogens.
•Pseudomonas•Acinetobacter•Burkholderia•Stenotrophomonas•NTB-Mycobacterium•Fungi Serving Customers Throughout North America
www.estechlab.com I 502-893-6080 I est@estechlab.com ��rK I Department of Health
�ATE
ELAP No. 12068
Stabilization of the Magnetite Layer in Steam Boilers With Tannins continued
Figure 4: (Left to right) Unpolished mild steel coupons—untreated, TG3304, TG3124, and TG3106 treatments. The colors observed give an indication of the thickness of the films (40).
Figure 5: Detached magnetite at the bottom of the reaction vessel of the autoclave.
Figure 6: Undulating oxide detaching from a surface. (Images from Reference 41.)
14
the Analyst Volume 27 Number 1
Deadly, but preventable. Add the reliable culture test for Legionella pneumophila to your customers’ water management plan to reduce the risk of Legionnaires’ disease.
You can reduce the risk. Learn more at idexx.com/lptesting.
© 2019 IDEXX Laboratories, Inc. All rights reserved. • 2184430-00 All ®/ TM marks are owned by IDEXX Laboratories, Inc. or its affiliates in the United States and/or other countries. The IDEXX Privacy Policy is available at idexx.com.
Stabilization of the Magnetite Layer in Steam Boilers With Tannins continued
In Potter and Mann’s experiments, up to half of the magnetite produced would fall away from the sample surfaces, but there is no indication that this happened by blistering (16). We have already mentioned that the Pilling-Bedworth ratio of magnetite (i.e., the ratio of the volume of the elementary cell of a magnetite to the volume of the elementary cell of iron) is 2.1 and that it is posited that the stresses that this volume expansion creates explain the random polycrystalline underlayer of Potter-Mann films. Could the compressive strain also explain the blisters? Huijbregts and Snel certainly showed this to be the case in a solution containing 0.1 M nickel chloride (NiCl) (see Figure 6) (41), but our own microscopic observations suggest an added mechanism, as will be seen below. Finally, the darker and duller appearance of the magnetite on the untreated coupon is indicative of a thicker layer of magnetite with a rough, light-dispersing surface. In the case of the tannin-treated coupons, the layer is smooth and shiny, and sometimes so thin as to create a bluish interference color. In the case of TG3124 treatment, it is so thin that it leaves visible some the sheen of the underlying metal.
GI-XRD As can be seen in Figure 7, GI-XRD allows us to identify the crystalline species present. In all cases, only the signature peaks of iron and magnetite were seen, but it is possible that small amounts of maghemite (γ-Fe2O3) are also present, as its peaks fall very close to those of magnetite. Traces of maghemite have been found in
16
boiler systems before (28) but would be inconsequential for our analysis. As can be seen in Figure 8, GI-XRD also allows for the determination of an average crystallite size by applying the Scherrer equation (Equation 2) to the largest magnetite peak. Equation 2 can be written as: τ = Kλ/βcosθ
Eq. 2
Where: τ = The mean size of the ordered (crystalline) domains, which may be smaller or equal to the grain size. K = A dimensionless shape factor, with a value close to unity. The shape factor has a typical value of about 0.9, but varies with the actual shape of the crystallite. λ = The X-ray wavelength. β = The line broadening at half the maximum intensity (FWHM), after subtracting the instrumental line broadening, in radians. This quantity is also sometimes denoted as Δ(2θ). θ = The Bragg angle. The average size of the tannin-treated sample is roughly half that of the untreated, a very significant difference if one considers that porosity of a compacted layer of small crystals will be much less than that of large crystals.
the Analyst Volume 27 Number 1
Stabilization of the Magnetite Layer in Steam Boilers With Tannins continued
Figure 7: The top diffractogram is taken on an untreated coupon oxidized in deoxygenated synthetic boiler water. The bottom one is taken on a coupon treated with TG3124 in deoxygenated synthetic boiler water. In both, only the peak characteristic of iron and magnetite can be seen. This is also the case for the diffractograms taken on TG3304 and TG3106 treated coupons. Notice that the peaks for the TG3124 are broader and shorter, indicating a smaller average crystal size.
17
the Analyst Volume 27 Number 1
Stabilization of the Magnetite Layer in Steam Boilers With Tannins continued
Figure 8: The top diffractogram, showing only the main magnetite peak, is taken on a coupon without treatment oxidized in deoxygenated synthetic boiler water, while the bottom one is from a coupon treated with TGWT 3124. The Scherrer equation allows us to extract the average size of the magnetite crystals: 31.17 nanometer (nm) for the untreated coupon, and 15.24 nm for the TG3124. These are the extremes seen in our experiments. TG3304 and TG3106 have intermediate sizes of 28.09 nm and 21.89 nm, respectively.
18
the Analyst Volume 27 Number 1
Stabilization of the Magnetite Layer in Steam Boilers With Tannins continued
SEM and EDS SEM reveals much more than just an average crystal size. It shows clearly and unsurprisingly that for the untreated sample, we have a Potter-Mann film, with large, well-formed crystals sitting mostly on top of a layer of smaller particles, having no clear crystalline morphology, as shown in the two images on the left in Figure 9. What is most surprising is the fact that for the tannin-treated sample, seen on the right in Figure 9, there is a complete absence of large-sized crystals on a much smoother surface. There are fewer defects, suggesting that the passivation layer is less porous and has stabilized enough to prevent further egress of iron from the metal surface to the surface of the oxide. Moreover, it can be seen in the untreated sample that small,well-formed crystals are lodged in cracks. Any growth of these is likely to disrupt the magnetite layer and participate in the process of blistering and spalling without having to create a large undulating structure.
Figure 9: (Left) The untreated coupon at medium and high magnifications. Notice the well-formed crystals lodged in cracks. Any growth of these will disrupt the magnetite layer. (Right) A tannin-treated coupon at the same magnifications. No large crystals are to be seen, which is an indication that there is no iron transport from the underlying metal to the surface.
“SEM reveals much more than just an average crystal size.� A further interesting observation on the untreated sample can be obtained by backscattered SEM imaging and EDS analysis of the blistered and unblistered zone. The image of the blistered zone appears darker, an indication of a smaller proportion of heavy elements, in this case iron. The measurements of the oxygen content yield the same unexpected result. There is more oxygen on the blistered zone when we would have expected less than in the magnetite-covered zone (see Figure 10). It would appear that the iron in the blistered zone has already undergone a first step in its oxidation back to magnetite, perhaps to maghemite, or more likely to hydroxides. This would support the mechanism of oxidation proposed by Carvalho and Kelly, shown in Figure 11 (9). Other spectroscopic techniques could confirm this hypothesis. Figure 10: The backscattered electron image at the top shows the border between the magnetite-covered region (left) and the blistered area (right). The elemental composition in the spectra below show 12.8% oxygen in the magnetite zone and 21.9% in the blistered zone, an unexpected result.
19
the Analyst Volume 27 Number 1
Stabilization of the Magnetite Layer in Steam Boilers With Tannins continued
Figure 11: Carvalho and Kelly’s suggested mechanism for the initial stages of magnetite film formation (9). The formation of hydroxides might explain the high percentage of oxygen seen by EDS in the blistered zone that resembles the bare metal surface.
Electrochemistry The experimental conditions for our measurements were extremely harsh, using 3.5% NaCl solutions. The results deal with worst-case scenarios for which steel parts would never be submitted, but are useful in comparing the passivation layers obtained by different treatments: Rest 1 hour (h) at open circuit potential (Eocp), which is close to the corrosion potential of the substrate. Potentiodynamic polarization from -25 millivolt (mV) to 1.5 volt (V) versus Eocp.
20
Electrochemical impedance spectroscopy was used to investigate the ability of a tannin/magnetite layer to slow down the corrosion rate of the underlying steel substrate: Potentiostatic EIS after 1h OCP from 100 kilohertz (kHz) to 10 megahertz (mHz), Ac 10 mV Figure 12 is useful in understanding what information can be gained from potentiodynamic measurements. Figure 13 shows the results for our experiments, namely a marked decrease in corrosion intensity for the TG3124 sample. In analyzing these results, it is good to keep in mind that the passivation layer for the tannin-treated sample is much thinner than the very thick but porous layer of the untreated sample.
the Analyst Volume 27 Number 1
Stabilization of the Magnetite Layer in Steam Boilers With Tannins continued
Figure 12: Typical information gained from potentiodynamic curves.
“The gradual increment of the impedance value in the tannin-treated samples suggests the formation of a protective passive oxide film on the steel surface.” Figure 13: Typical potentiodynamic curves for the bare metal sample as-received, the untreated oxidized sample, and two tannin-treated samples. The arrow indicates a decrease in corrosion intensity (corrosion current).
Figure 14 shows typical impedance-frequency Bode plots: the impedance at the lowest studied frequency (0.01 Hz) varies with the treatment. The gradual increment of the impedance value in the tannin-treated samples suggests the formation of a protective passive oxide film on the steel surface.
21
the Analyst Volume 27 Number 1
Stabilization of the Magnetite Layer in Steam Boilers With Tannins continued
Figure 14: Impedance-frequency Bode plots for the bare metal sample asreceived, the untreated oxidized sample, and two tannin-treated samples.
Finally, Figure 15 shows frequency-phase Bode plots. The maximum phase angle for all four materials in service environment exposure is between 50° and 60°, respectively, and lesser for the base metal. Also, the maximum angle value is shifted toward lower frequencies (5 Hz for as-received material, and between 1 Hz to 0.3 Hz for tested samples). The shifting of the phase angle at the lower frequency is attributed to the formation of doublelayer capacitance and the reduction in the anodic surface area of substrate. This phenomenon indicates that the surface was covered with protective and thick passive layers. Finally, the high frequency values of the phase for bare, TG3124, TG3106, and unprotected metal show that the system behaves like a pure resistance being the electrolyte resistance. This, combined with the low-|Z| value for the same high frequency, demonstrates that the saltwater solution comes in contact with the metal.
Figure 15: Frequency-phase Bode plots for the bare metal sample asreceived, the untreated oxidized sample, and two tannin-treated samples.
22
the Analyst Volume 27 Number 1
Stabilization of the Magnetite Layer in Steam Boilers With Tannins continued
Hydrogen Evolution in Tannin-Treated Boilers Although we did not monitor the amount of hydrogen produced in our experiments, the larger amount of magnetite (both adhered and spalled) on the untreated sample indicates that this byproduct of the Schikorr reaction was more abundant. The thinner layers of magnetite on the tannin-treated samples indicates either an overall lower rate of the reaction throughout the 96-hour experiments, or, more likely, a reduced rate after a certain thickness of a denser, less porous magnetite film is formed in the presence of tannins. Supporting this hypothesis is data from an industrial boiler shown in Figure 16. Soon after the water treatment is switched from a conventional one to tannins, the level of hydrogen in the steam drops, indicating that tannins reduce the rate of the Schikorr reaction. Figure 16: Hydrogen measurements in the steam of a boiler before and after initiating a tannin-based treatment at the time indicated by the red arrow.
Concluding Remarks and Further Work
Recent understanding of the mechanism by which tannins protect mild steel boiler surfaces came from the work of Dargahi, et al. (42, 43), who showed, by measurements in a quartz-crystal microbalance with dissipation (QCM-D), that tannins adsorb on mild steel (see Figure 17). Electrochemical impedance spectroscopy measurements showing improved corrosion resistance supported the hypothesis that an iron-tannate film was the source of the passivation. Though this may be the case for closed loops, it is unlikely that the same situation applies to boilers in which magnetite is always found on the surfaces.
23
Figure 17: Adsorption isotherm for a tannin-based inhibitor onto mild steel at pH 10.5 and room temperature. Circles represent the experimental data, while the solid line represents the corresponding value from the Langmuir isotherm. Inset: experimental data (circles) show an excellent correlation with the linearized Langmuir isotherm (from Reference 43).
the Analyst Volume 27 Number 1
Stabilization of the Magnetite Layer in Steam Boilers With Tannins continued
The data presented in this article suggests that we have another phenomenon at work that allows us to present an alternate model to explain the effect of tannins in boilers (see Figure 18). Adsorption of tannins on steel does not prevent an underlying magnetite film from forming but affects its structure by stabilizing it in the following ways: 1. A single layer of magnetite is produced with a reduced thickness. 2. The crystal size in this layer is greatly diminished, as also is the porosity. 3. Spalling and blistering are eliminated, indicative of an improved adhesiveness to the metal. 4. Migration of iron from the base layer of metal is stopped. 5. Hydrogen production is reduced. 6. Resistance to corrosion is improved.
Further work will hopefully reveal the mechanism by which this happens, but in view of the likely models by which magnetite is produced (outlined in our introduction), the most probable hypothesis is that pore-blocking plays a critical role. Key questions to be answered are: 1. Does this happen only at the surface, or throughout the porous magnetite structure as it evolves? 2. Does it occur by adsorption or by precipitation of iron-tannate complexes inside the pores? The answers to these questions would help to explain the process and role that tannins play.
Figure 18: (Top) A cartoon representing the previous model to explain the improved corrosion resistance when tannins are used. (Bottom) A cartoon representing the stabilization of the magnetite layer by tannins to explain the improved corrosion resistance.
24
the Analyst Volume 27 Number 1
Stabilization of the Magnetite Layer in Steam Boilers With Tannins continued
Acknowledgements
This project was realized with the help of the Engage Program of the Natural Sciences and Engineering Research Council of Canada (NSERC), in partnership with the Centre de Métallurgie du Québec. LouisPhilippe Cloutier and Richard Delisle of TGWT were instrumental in providing useful insights, comments, and suggestions. The authors also wish to thank Sofiene Amira for help in initiating the project and for technical help. Finally, Kokou Assogba’s technical help in the lab was essential to the project.
References
1. Keir, J. (1790). “Experiments and observations on the dissolution of metals in acids, and their precipitations; with an account of a new compound acid menstruum, useful in some technical operations of parting metals,” Philosophical Transactions of the Royal Society of London, 1790(80): pp. 359-384. 2. Schönbein, C.F.; Faraday, M. ( June 17, 1836). “On a Peculiar Voltaic Condition of Iron,” Richard Taylor, Lion Red Court, Fleet Street.
3. Davenport, A.J.; Oblonsky, L.J.; Ryan, M.P.; Toney, M.F. (2000). “The Structure of the Passive Film that Forms on Iron in Aqueous Environments,” Journal of the Electrochemical Society 147(6), pp. 2162-2173.
4. Bragg, W. (1915). “The Structure of Magnetite and the Spinels,” Nature 95(2386), p. 561.
5. Wu, W.; Wu, Z.; Yu, T.; Jiang, C.; Kim, W.S. (2015). “Recent Progress on Magnetic Iron Oxide Nanoparticles: Synthesis, Surface Functional Strategies and Biomedical Applications,” Science and Technology of Advanced Materials 16(2), p. 023501. 6. Moore, J.B.; Jones, R.L. (1968). “Growth Characteristics of Iron Oxide Films Generated in Dilute Lithium Hydroxide Solution at 300°C,” Journal of The Electrochemical Society 115(6), pp. 576-583.
7. Schikorr, G. (1933). “Über Eisen (II)‐hydroxyd und ein ferromagnetisches Eisen (III) hydroxyd,” Zeitschrift für anorganische und allgemeine Chemie 212(1) (“About Iron (II) Hydroxide and a Ferromagnetic Iron (III) Hydroxide,” Journal of Inorganic and General Chemistry), pp. 33-39. 8. Noack, M. (April 17-21, 1989). “Oxygen Scavengers,” presentation at Corrosion '89, New Orleans, LA. New Orleans, LA.
9. Carvalho, L.; Kelly, J.A. (March 6-30, 2016). “The Chemistry and Crystallographic Characteristics of Passive Magnetite Film Formation,” presented at Corrosion 2016, Vancouver, B.C., Canada. 10. Roubaty, J. (1986). “La corrosion des chaudières; son suivi par l'analyse de l'hydrogène dans la vapeur,” La Technique modern 78(1-2) (“Corrosion of Boilers; Followed by the Analysis of Hydrogen in Vapor,” Modern Technology 78(1-2)), pp. 17-20.
11. Bloom, M.; Krulfeld, M. (1957). “A Hydrogen Effusion Method for the Determination of Corrosion Rates in Aqueous Systems at Elevated Temperature and Pressure,” Journal of the Electrochemical Society 104(5), pp. 264-269.
12. Potter, E. (1961). “Oxidation of Mild Steel in High-Temperature Aqueous Systems,” Proceedings of the 1st International Congress on Metallic Corrosion, London, UK, pp. 417-426. 13. Potter, E. (1963). “Mechanism of Magnetite Growth on Low-Carbon Steel in Steam and Aqueous Solutions up to 550°C,” in Proceedings of the 2nd International Congress on Metallic Corrosion, Houston, TX.
14. Potter, E. (1962). The First International Congress on Metallic Corrosion, 1961, Butterworths, London, 712 pages, Pergamon.
15. Bloom, M.; Newport, G.; Fraser, W. (1964). “Steel Corrosion Mechanisms: The Growth and Breakdown of Protective Films in High-Temperature Aqueous Systems at 316°C,” Journal of The Electrochemical Society 111(12), pp. 1343-1347. 16. Potter, E.; Mann, G. (1965). “The Fast Linear Growth of Magnetite on Mild Steel in High-Temperature Aqueous Conditions,” British Corrosion Journal 1(1), pp. 26-35.
25
17. Castle, J.; Mann, G. (1966). “The Mechanism of Formation of a Porous Oxide Film on Steel,” Corrosion Science 6(6), pp. 253-262.
18. Castle, J.; Masterson, H. (1966). “The Role of Diffusion in the Oxidation of Mild Steel in High-Temperature Aqueous Solutions,” Corrosion Science 6(3-4), pp. 93-104.
19. Marsh, T. (1966). “The Morphology of Magnetite Growth on Mild Steel in Alkaline Solutions at 316°C,” Journal of the Electrochemical Society 113(4), pp. 313-318. 20. Field, E.M.; Holmes, D. (1965). “Nucleation and Growth of Magnetite Films on Pure Iron in High-Temperature Water,” Corrosion Science 5(5), pp. 361-370.
21. Friggens, H.A.; Holmes, D. (1968) “Nucleation and Growth of Magnetite Films on Fe in High-Temperature Water,” Corrosion Science 8(12), pp. 871-881.
22. Robertson, J., (1989) “The Mechanism of High-Temperature Aqueous Corrosion of Steel,” Corrosion Science 29(11-12), pp. 1275-1291.
23. Robertson, J.; Manning, M. (1988). “Criteria for Formation of Single Layer, Duplex, and Breakaway Scales on Steels,” Materials Science and Technology 4(12), pp. 1064-1071.
24. Bignold, G.; Garnsey, R.; Mann, G. (1972) “High-Temperature Aqueous Corrosion of Iron Development of Theories of Equilibrium Solution Phase Transport through a Porous Oxide,” Corrosion Science 12(4), pp. 325-332.
25. Berge, P.; Ribon, C.; Paul, P.S. (1977). “Effect of Hydrogen on the Corrosion of Steels in High-Temperature Water,” Corrosion 33(5), pp. 173-178.
26. Sánchez-Moreno, M.; Takenoutib, H.; García-Jareñoc, J.J.; Vicentec, F.; Alonsoa, C. “A Theoretical Approach of Impedance Spectroscopy during the Passivation of Steel in Alkaline Media,” Electrochimica Acta, 54(28), pp. 7222-7226.
27. Xu, W.; Daub, K.; Zhang, X.; Noel, J.J.; Shoesmith, D.W.; Wren, J.C. (2009). “Oxide Formation and Conversion on Carbon Steel in Mildly Basic Solutions,” Electrochimica Acta 54(24), pp. 5727-5738.
28. Namduri, H.; Nasrazadani, S. (2008). “Quantitative Analysis of Iron Oxides Using Fourier Transform Infrared Spectrophotometry,” Corrosion Science 50(9), pp. 2493-2497.
29. Kumai, C.S.; Devine, T.M. (2005). “Oxidation of Iron in 288°C Oxygen-Containing Water,” Corrosion 61(3), pp. 201-218.
30. Tomlinson, L. (1981). “Mechanism of Corrosion of Carbon and Low-Alloy Ferritic Steels by High-Temperature Water,” Corrosion 37(10), pp. 591-596.
31. Cheng, Y.; Steward, F. (2004). “Corrosion of Carbon Steels in High-Temperature Water Studied by Electrochemical Techniques,” Corrosion Science 46(10), pp. 2405-2420.
32. Shibata, T.; Watanabe, M.; Taniguchi, N.; Shimizu, A. (September 2014). “Modelling of Carbon Steel Corrosion under an Oxygen-Depleted Environment,” Corrosion Engineering, Science and Technology 49(6), pp. 435-441.
33. Bornak, W. (1988). “Chemistry of Iron and its Corrosion Products in Boiler Systems,” Corrosion 44(3), pp. 154-158.
34. Joshi, P.; Venkateswaran, G.; Venkateswarlu, K. (1992). “Chelant Enhanced Passivation of Carbon Steel in Deoxygenated Alkaline Aqueous Solutions,” British Corrosion Journal 27(3), pp. 200-206.
35. Joshi, P.; Venkateswaran, G.; Venkateswarlu, K. (1992). “Passivation Behavior of Carbon Steel Alloy in the Presence of EDTA, Ni (II) EDTA, and LiOH at 473°K,” Corrosion 48(6), pp. 501-508.
36. Tvedt, T.; Wallace, S.; Griffin Jr., F. (1983). “Evaluation of On-Line Chelant Addition to PWR Steam Generators,” steam generator cleaning project, Dow Chemical Co., Midland, MI.
37. Tvedt, T.; Wallace, S. (1987). “Chelant Passivation: New Study Challenges an Old Myth,” Power 131(2).
38. Topp, H.; Hater, W.; Bache, A.B.; Kolk, C. ( January 2012). “Film-Forming Amine in Shell Boilers,” PowerPlant Chemistry 14(1), pp. 38-48.
39. Song, G.-D.; Jeon, S.-H.; Kim, J.-G.; Hur, D.-H. (August 2016). “Effect of Polyacrylic Acid on the Corrosion Behavior of Carbon Steel and Magnetite in Alkaline Aqueous Solutions,” Corrosion 72(8), pp. 1010-1020.
the Analyst Volume 27 Number 1
Stabilization of the Magnetite Layer in Steam Boilers With Tannins continued
40. Burleigh, T.D.; Dotson, T.C.; Dotson, K.T.; Gabay, J.; Sloan, T.B.; Ferrell, S.G. ( January 2007). “Anodizing Steel in KOH and NaOH Solutions,” Journal of the Electrochemical Society 154(10), pp. C579-C586. 41. Huijbregts, W.; Snel, A. (1972). “The Protection Effectiveness of Magnetite Layers in Relation to Boiler Corrosion”: in 5th International Congress on Metallic Corrosion, Tokyo, Japan.
42. Dargahi, M.: Gaudreault, R.; Olsson, A.L.J.; Tufenkji, N. (Oct. 29-Nov. 1, 2014). “Green Chemistry: Purified Tannin Molecules for the Protection of Mild-Steel Closed-Loop Systems,” technical paper presentation at the 2014 annual AWT Conference, Fort Worth, TX. 43. Dargahi, M.; Gaudreault, R.; Olsson, A.L.J.; Tufenkji, N. (November 2015). “Green Technology: Tannin-Based Corrosion Inhibitor for Protection of Mild Steel,” Corrosion 71(11), pp. 1321-1329.
Endnote The tannin solutions used in the research came from TGWT Clean Technologies. Formulations used included TG 3106, TG 3124, and TG 3304.
A
Louis Godbout worked as a research assistant and academic associate at McGill University’s Pulp and Paper Research Center for more than 20 years before joining TGWT Clean Technologies in 2016. He was one of the pioneers in the field of nanocrystalline cellulose research. Mr. Godbout developed several patents and published many articles on these materials as well as on the fundamental structure of the native cellulose crystal. Mr. Godbout has also been active in the field of scientific education. He is a volunteer on the STEM task force of the Association of Water Technologies. He can be reached at lgodbout@tgwt.com.
Axel Gambou-Bosca. Ph.D., is an R&D project manager at the Quebec Metallurgy Center, a technology transfer center affiliated to the “Cégep de Trois-Rivières.” His work focuses on electrochemistry, corrosion, and surface science and touches on various industries. He is constantly working on providing knowledge, guidance, and solutions to mitigate in-service failure due to corrosion attack. Dr. Gambou-Bosca holds a Ph.D. in electrochemistry from the Université du Québec à Montréal. He may be reached at axel.gambou.bosca@cegeptr.qc.ca. Christian Fowelin, Ph.D., is the head of R&D at Korn GmbH in Hamburg, Germany. He has more than 10 years of experience in the field of boiler water and cooling water treatment and dedicates his research to the further development of green chemistry aspects in industrial water applications. Dr. Fowelin studied chemistry at the University of Hamburg, where his research interests included metal organic complexes with ligands on the bases of modified naturally available amino sugars. He received his doctorate (Dr. rer. nat., summa cum laude) in 2009. Dr. Fowelin can be reached at cfowelin@tgwt.com. This technical paper was presented at the 2019 AWT Annual Conference, which was conducted September 11–14, 2019, in Palm Springs, California.
AWT Business Owners Meeting February 10-11, 2020 • Clearwater, FL
Thank You to Our Sponsors Gold
Silver
26
the Analyst Volume 27 Number 1
Bronze
AMSA BCP Products TM
Clean it Up & Keep it Clean
TM
Use BCPTM biodispersants as part of a Biofilm Control Program with a continual low dose.
Use BCPTM biodispersants to clean up a fouled system with a slug dose treatment.
• Penetrate
• Prevent
& disperse surface deposits • Clean up surfaces when starting a laid-up system in the spring • Achieve on-line cleaning in hard to reach fill and dead leg areas • Give circulating water systems an extra cleaning before winter shut-down
AMSA, Inc.® 4714 S. Garfield Rd. Auburn, Michigan 48611 Tel: (989) 662-0377 Fax: (989) 662-6461 sales@amsainc.com www.amsainc.com
surface deposit formation
• Prevent
microbial induced corrosion
• Extend
scale & corrosion inhibitor package
• Reduce
BCP
TM
biocide use with products
Call Us Today! 888 739-0377
For a Clean Industrial Cooling Water System
Can Induction Time Methods Aid in Evaluation of Calcium Carbonate and Calcium Phosphate Scale Inhibitors? Bill Glover, Ph.D., and Kaylie L. Young, Ph.D. (Dow Chemical), and Robert J. Ferguson (French Creek Software)
Photo courtesy of David Daniels.
Introduction
Scale-inhibitor testing in the laboratory is the first step in providing reliable information for comparing the efficacy of scale inhibitors of different chemistries and between different manufacturers. Unfortunately, the laboratory tests and the reporting of results are not standardized across the industry, so each scale-inhibitor manufacturer is free to choose arbitrary conditions under which they conduct their testing. Although not maliciously misleading, the testing may present a limited view of the product performance. In addition, the results are often presented as percent inhibition, which besides being calculated in several different manners by different groups, does not necessarily provide a true representation of the performance of a scale inhibitor under real-world conditions, as the duration of the test can be either too short or too long to model residence times in actual systems using water as a heat transfer medium (1). This article presents efforts to develop methods for the evaluation of scale inhibitors for two of the most common scales: calcium carbonate and calcium phosphate. The use of induction time, or the onset of scale formation in the system, has several key advantages. The first is that time is a variable that is accounted for. As most people in the industry are aware, the function of a scale inhibitor is to delay the onset of scaling, not to prevent it altogether (1). The onset of scaling needs to be delayed until the water has safely passed through the system (2). The saturation conditions encountered in real-world systems and mimicked in the experimental procedures are such that the thermodynamics of the system ensure that scale will form. The induction time testing provides an idea of the kinetics, or the length of time until scale starts forming. The second advantage is that scale-inhibitor dosages can be modeled as a function of the residence time to avoid under or overdosing. The synergistic or antagonistic interactions of different components or additives can also be readily studied and modeled. The last advantage is that the upper limits of the inhibitory action of the product can be determined, providing a clearer understanding of the point of product failure (3). As noted, scale inhibitors are employed in the water treatment industry to delay the onset of scale formation through the prevention of nucleation growth of the scale particle beyond a critically sized cluster (1). By doing such, the saturated waters are allowed time to be 29
removed from the system and no longer pose a scaling hazard (2). Although several models for the induction time or time for the onset of the formation of scale have been proposed, the most intuitive can be represented as in Equation 1 (3): Time = 1/K [SR-1] P-1
Eq. 1
Where: Time = induction time K = a directly correlated temperature dependent rate constant SR = saturation ratio P = the number of molecules in a critically sized cluster
“Scale inhibitors are employed in the water treatment industry to delay the onset of scale formation.� From Equation 1, several correlations can be drawn. The first is that the smaller or the shorter the induction time, the quicker scale forms in the system. The second is that the induction time is inversely correlated to the temperature and saturation ratio. Models for untreated induction time are used to evaluate if scale is expected during the water’s residence time in the system, and as baseline induction time for some induction time extension models (4). However, Equation 1 does not account for the potential effect that a scale inhibitor may have on the system. Taking into account the scale inhibitor, the induction time equation can be re-written as Equation 2 (3): Time = [inhibitor]M / K [SR-1] P-1
Eq. 2
Where: Time = induction time K = a temperature-dependent rate constant SR = saturation ratio P = the number of molecules in a critically sized cluster. [Inhibitor] = the molar concentration of the scale inhibitor M = coefficient related to the ratio of inhibitor molecules to a critical cluster the Analyst Volume 27 Number 1
Can Induction Time Methods Aid in Evaluation of Calcium Carbonate and Calcium Phosphate Scale Inhibitors? continued
From Equation 2, it is clear at first glance, the inhibitor concentration is directly correlated to an increased induction time. What is not clear, and can only be determined through experimentation because they are dependent on the chemistry of the scale inhibitor, is the minimum effective dosage of scale inhibitor at a given saturation ratio and the point of failure where no amount of scale inhibitor can prevent the formation of scale for a reasonable time period.
Experimental Procedure
The calcium carbonate and calcium phosphate induction time tests developed rely on different detection mechanisms. Induction time for calcium carbonate scale formation can be measured by monitoring the pH of the system. It is well known that at the time of calcium carbonate scale formation, some amount of carbonate/bicarbonate will be consumed, and it will shift the calco-carbonic equilibrium toward the acid forms, resulting in a decrease in the pH of the system. Thus, continuous monitoring of the pH of the system after mixing solutions of calcium chloride and sodium carbonate and sodium bicarbonate, resulting in a desired supersaturation of calcium carbonate, will allow for a measurement of the induction time. The calcium phosphate test relies on an increase in turbidity as the phosphate scale forms. Calcium carbonate induction time by pH. The first steps in the experimental design are to determine the saturation ratio at temperatures at which one wishes to conduct the experiments. The temperatures are typically run between 20 째C and 80 째C to account for the possible range of bulk water and film temperatures encountered in a typical cooling system. The concentration of reagents to add to achieve a desired saturation ratio can be estimated with the help of appropriate predictive software. Typical ranges for calcite saturation are 30 to 250X saturation. Most inhibitors fail between 135 and 150X saturation. In these experiments, the saturation ratios of 60X, 90X, and 150X were tested at 22 째C. Previous studies have noted that it may be desirable to run the experiments over a range of pH values to account
30
for inhibitor dissociation, but this was not done in these experiments. The standard stock polymer solutions (1,000 parts per million [ppm] by actives) were pH-adjusted to 8.0 so as to not alter the pH significantly when added to the supersaturated solutions. Two test solutions were prepared to achieve the desired saturation ratios. Solution A consisted of 600-ppm calcium as calcium carbonate and was used for each saturation index. Solution B differed for each saturation ratio and consisted of a solution of sodium carbonate and sodium bicarbonate in the approximate ratio of 1:5. Placed into a 125-milliliter (mL) glass jar were 50 mL of Solution A, 40 mL of water with the desired concentration of inhibitor, and a magnetic stir bar. The jar was placed on a magnetic stir plate and a pH probe inserted into the solution. A few data points are collected to ensure the probe is working properly, at which time 10 mL of Solution A is added. The pH was instantly observed to drop to a pH of about 8.6. Readings are periodically taken until the pH drops from 8.6. Specifically, the induction time was estimated to be the time point at which the pH drops outside the standard deviation of the flat portion of the curve at 8.6, since this marks the formation of a new phase (calcium carbonate [CaCO3] scale). Scaling experiments are prone to poor reproducibility because of differences in scale nucleation for each experiment. It is therefore essential to try to minimize variability in the method and materials used. Calcium phosphate induction time by turbidity. Again, the first steps in the experimental design are to determine the saturation ratio and temperatures at which one wishes to conduct the experiments. The temperatures in these experiments were run at 22 째C, as the ability to control the temperature at a higher point was lacking with the experimental apparatus. The saturation ratio can be estimated with the help of appropriate predictive software. Two sets of conditions were chosen to mimic possible municipal effluent reuse conditions as depicted in Table A.
the Analyst Volume 27 Number 1
Can Induction Time Methods Aid in Evaluation of Calcium Carbonate and Calcium Phosphate Scale Inhibitors? continued
Table A: Solution Concentrations for Calcium Phosphate Induction Time Experiments Component
Condition 1
Condition 2
Alkalinity
Solution Type
Sodium bicarbonate (NaHCO3)
200 ppm as CaCO3
200 ppm as CaCO3
Phosphate
Sodium biphosphate (Na2HPO3)
40 ppm PO4
100 ppm PO4
Hardness
Calcium chloride (CaCl2*2H2O) Magnesium chloride (MgCl2*6H2O)
4,000 ppm Ca as CaCO3 2,000 ppm Mg as CaCO3
200 ppm Ca as CaCO3 100 ppm Mg as CaCO3
Polymer
10 ppm as actives
10 ppm as actives
--
4,037
6,339
Inhibitor Calcium phosphate saturation index (calculated)
The solution concentrations for the calcium phosphate induction time experiments were chosen to represent two typical scenarios encountered. Condition 1 represents water to be treated with high hardness levels and moderate phosphate levels, while Condition 2 represents a scenario of moderate hardness and high phosphate levels. Placed into a 125-mL sample vial and mixed were 40 mL of alkalinity solution, 20 mL of phosphate solution, 1 mL of inhibitor stock solution (1,000 ppm as actives), and a small magnetic stir bar. 40 mL of the hardness solution was then added, and the vial was quickly inverted 25 times for mixing. The vial was then inserted into the turbidity meter, as shown in Photo 1, and the drive for the magnetically coupled stirrer engaged. The turbidity of the solution was read approximately 1 centimeter (cm) above the stir bar. Turbidity of the water was measured until it reached 5 Nephelometric Turbidity Units (NTU), which was arbitrarily chosen as the endpoint for these experiments.
Representative Examples of Experimental Results Calcium Carbonate Induction Time Figure 1 shows the data for a blank, which contains no inhibitor, conducted at 60X the saturation ratio. The pH drop after 30 seconds indicates the addition of Solution B. The drop in the pH curve at about 150 seconds provides a general reference point for the graphs that follow. Figure 1: Calcium carbonate induction time for solution without inhibitor at 60X saturation ratio.
Photo 1: Modified Microtol turbidity meter.
Figure 2 shows the data for a blank and a modified acrylic acid homopolymer tested under conditions of 60X saturation and 0.5 ppm inhibitor. The data shows that the pH of the solution with the inhibitor does not drop for over 50,000 seconds, showing that at this saturation ratio, even a low dose of the inhibitor can effectively inhibit calcium carbonate scale for an extended period of time.
31
the Analyst Volume 27 Number 1
Can Induction Time Methods Aid in Evaluation of Calcium Carbonate and Calcium Phosphate Scale Inhibitors? continued
Figure 2: Calcium carbonate induction time for 0.5 ppm modified acrylic acid inhibitor at 60X saturation ratio.
Figure 4: Calcium carbonate induction time for 1 ppm modified acrylic acid inhibitor at 150X saturation ratio.
Figure 3 shows the data for a blank and a modified acrylic acid homopolymer tested under conditions of 90X saturation and 1 ppm inhibitor. The data shows that the pH of the solution with the inhibitor does not drop for more than 14,000 seconds, showing that at this moderate saturation ratio, a relatively low dose of the inhibitor can effectively inhibit calcium carbonate scale for an extended period of time.
Condition 1 Figures 5 through 7 graphically show data from treatment Condition 1.
Figure 3: Calcium carbonate induction time for 1 ppm modified acrylic acid inhibitor at 90X saturation ratio.
Calcium phosphate induction time. Figure 5 shows the data for a blank and an acrylic acid homopolymer tested under Condition 1. The data closely track each other, indicating that, as expected, an acrylic homopolymer is not an effective calcium phosphate scale inhibitor. Both the blank and the homopolymer solutions reach 5 NTU in about one and a half minutes. The break in the curve that occurs at ~10 NTU is the result of a detector changeover in the turbidimeter. Figure 5: Calcium phosphate induction time for acrylic homopolymer under Condition 1.
Figure 4 shows the data for a blank and a modified acrylic acid homopolymer tested under conditions of 150X saturation and 1 ppm inhibitor. The data shows that the pH of the solution with the inhibitor does not drop for over 400 seconds. As expected, the induction time is shorter at 150X than 90X at the same inhibitor concentration.
32
Figure 6 compares the data under test Condition 1 for the blank and an AA/AMPS copolymer. The terpolymer functions much more effectively as a calcium phosphate scale inhibitor. The copolymer solution reaches 5 NTU in about 15 minutes as compared to 1.5 minutes for the blank. the Analyst Volume 27 Number 1
Innovating Water Hygiene
Point of Use Filters Patented Monochloramine Disinfection Technologies Water Safety Plans Legionella Testing
Providing all the right tools to water treatment professionals
Join the Sanipur All-Star Team +1-484-351-8702 w w w. san i p u r. co m sales@sanipur.com
Can Induction Time Methods Aid in Evaluation of Calcium Carbonate and Calcium Phosphate Scale Inhibitors? continued
Figure 6: Calcium phosphate induction time for acrylic acid/AMPS copolymer under Condition 1.
Figure 8: Calcium phosphate induction time for acrylic homopolymer under Condition 2.
Figure 7 compares the data under test Condition 1 for the blank and an AA/AMPS/nonionic monomer terpolymer. The copolymer functions much more effectively as a calcium phosphate scale inhibitor. The terpolymer solution reaches 5 NTU in about 24 minutes as compared to 1.5 minutes for the blank, indicating that it is an even more effective calcium phosphate scale inhibitor under these conditions. Figure 7: Calcium phosphate induction time for acrylic acid/AMPS/nonionic monomer terpolymer under Condition 1.
Figure 9 compares the data under test Condition 2 for the blank and an AA/AMPS copolymer. The copolymer functions much more effectively as a calcium phosphate scale inhibitor. The copolymer solution reaches 5 NTU in about 67 minutes as compared to 1 minute for the blank. Figure 9: Calcium phosphate induction time for acrylic acid/AMPS copolymer under Condition 2.
Condition 2 Figure 8 shows the data for a blank and an acrylic acid homopolymer tested under Condition 2. In this case, the data does not closely track each other and the acrylic acid homopolymer is an effective scale inhibitor. The blank scales almost immediately and reaches 5 NTU in about a minute, while the homopolymer solution does not scale and reach 5 NTU for about 28 minutes. 34
Figure 10 compares the data under test Condition 2 for the blank and an AA/AMPS/nonionic monomer terpolymer. The terpolymer functions much more effectively as a calcium phosphate scale inhibitor. The terpolymer solution does not reach 5 NTU, even after 90 minutes of testing, indicating that it is an even more effective calcium phosphate scale inhibitor under these conditions. the Analyst Volume 27 Number 1
NOT JUST CHEMICALS, WE PROVIDE SOLUTIONS The right water treatment chemical program can help optimize energy and water management for your customers. Brenntag offers the broadest range of treatment options. Our technicians are part of a global network that can help create innovative solutions for each application. ■ In-house network of technical professionals ■ Global footprint and sourcing capabilities ■ Ability to bring knowledge to the marketplace Water is life - that’s why we care To learn more about Brenntag, visit brenntagwater.com, email contactus@brenntag.com, or call (800) 890-0355.
Phosphonates, Polymeric scale inhibitors, Corrosion Inhibitors, Heavy Metal Removal, Coagulants, Flocculants, Bioaugmentation, Biocides and Disinfectants, Chlorine Dioxide, Defoamers, Filtration Media, Glycols, Ion Exchange Resins, Odor Control, Permanganates, Acids and Alkalis, Activated Carbon
Can Induction Time Methods Aid in Evaluation of Calcium Carbonate and Calcium Phosphate Scale Inhibitors? continued
Figure 10: Calcium phosphate induction time for acrylic acid/AMPS/nonionic monomer terpolymer under Condition 2.
Modelling Induction Time
Untreated induction time. Equation 1 can be used to develop models for predicting untreated induction time from data such as test blanks. Taking the log of both sides of the equation linearizes the relationship for regression analysis of the data and Substituting an Arrhenius relationship from Equation 3 for rate constant K, we arrive at Equation 4. K = A e -Ea/RT
Eq. 3
Figure 11: Predicted untreated induction time values from a simple model that can indicate whether or not scale formation will occur.
Induction Time Extension The impact of inhibitors on induction time can be modeled by applying the same procedure used to model untreated induction time to Equation 2 for extended induction time, as illustrated in Equation 5. Log(time) = Eq. 5 M x log(Inhibitor) + log A – Ea/(RT) – (1-P) x log(SR-1) 1 Improved correlations are obtained when the dissociated inhibitor concentration is used rather than the total inhibitor dosage (3, 4).
Where: A = represents the frequency of molecular collision Ea = the Activation Energy R = the Gas Constant T = Absolute Temperature
A combination equation using Equation 2 and Equation 3 can also be used, as shown in Equation 6.
Log(time) = log (A) – Ea/(RT) – (1-P) x log(SR-1) Eq. 4
A form of Equation 6 was developed at the Rice University Brine Consortium (5).
Figure 11 profiles predicted untreated induction time values from a simple model developed from blanks for the calcite induction time extension and minimum effective inhibitor dosage test. Untreated induction time indicates whether or not scale formation will commence before the water has passed through the system or perturbed state. It can also be used as the base for induction time extension models.
Total Induction Time = Eq. 6 Base Untreated Induction Time + Treated Extension
Figure 12 profiles induction time versus polymer dosage for a calcite model developed from Equation 5 and induction time test data. The coefficients for the baseline and treated models represent inhibitor-elicited changes in Activation Energy, Ea, and number of molecules P as indicators of inhibitor impact on seed formation and growth (6).
“Untreated induction time indicates whether or not scale formation will commence before the water has passed through the system.” 36
the Analyst Volume 27 Number 1
Can Induction Time Methods Aid in Evaluation of Calcium Carbonate and Calcium Phosphate Scale Inhibitors? continued
Figure 12: The graph illustrates Equation 5.
Bill Glover, Ph.D., holds a B.A. from Thiel College and an M.S. and doctorate in analytical chemistry from Louisiana State University. Dr. Glover has 30 years of experience in industrial water treatment, wastewater, and aquaculture in roles including formulations chemist, plant manager, sales, logistics, and technical service. His current role is a technical service and development specialist with Dow, serving customers in the industrial water and mining industries. He can be reached at WGlover@dow.com.
Summary
In this article, two methods for experimentally determining the induction time, or time for the onset of scaling, were presented for both calcium carbonate and calcium phosphate scales. These methods have found general applicability for a range of experimental conditions, including variations in saturation ratio and inhibitor concentration. Representative examples of experimental results were shown that can help water treatment professionals dose systems in an effective and cost-efficient manner. Data modeling methods were outlined to allow model development using standard linear regression. The methods will also be useful for researchers in comparing chemistries and determining minimum inhibitory concentrations for their formulations.
References
1. Ferguson, R.J. (Sept. 14–17, 2011. “The Kinetics of Cooling Water Scale Formation and Control,” Association of Water Technologies Annual Conference, Atlanta, Georgia. 2. Ferguson, R.J. (Nov. 1992). “Developing Scale-Inhibitor Models,” WATERTECH, Houston, Texas.
3. Ferguson, R.J.; Standish, C. (Sept. 13–16, 2017). “Developing Realistic Scale Inhibitor Test Procedures: Calcium Carbonate Scale Inhibitor Testing,” Association of Water Technologies Annual Conference, Grand Rapids, Michigan.
4. Ferguson, R.J. (Feb. 9–12, 2015). “The Impact of Inhibitor Speciation on Efficacy: pH, Ionic Strength, and Temperature Impact,” Cooling Technology Institute Annual Conference, New Orleans, Louisiana.
5. Tomson, M.B.; Fu, G.; Watson, M.A.; Kan, A.T. (2002). "Mechanisms of Mineral Scale Inhibition,” Society of Petroleum Engineers, Oilfield Scale Symposium, Aberdeen, UK.
Kaylie Young, Ph.D., is currently a staff scientist on the Oilfield Chemicals Water RD&E Team at Nalco Champion, an Ecolab Company, based in Sugar Land, Texas. When this paper was written, Dr. Young was an associate chemist with Dow Chemical and was the platform lead for the global Water Treatment Sciences team. She led the development of an innovation pipeline for the group. Before that she was part of the Phase Separation R&D Team at Dow, where she concentrated on the development of new polymeric reverse emulsion breakers for oilfield applications. Dr. Young holds a B.S. from Brown University and a Ph.D. in materials chemistry from Northwestern University. She can be reached at kaylie. young@ecolab.com. Robert J. Ferguson is the president of French Creek Software, Inc., a company he co-founded in 1989. His professional career includes positions with Nalco, Apollo, Mogul, Calgon, Chemlink, and Baker. Mr. Ferguson began modeling mineral scale formation and its control in 1974. Software he has developed is used for modeling cooling water, reverse osmosis, and oil field chemistry. He was educated at the U.S. Naval Academy and the University of Minnesota and received a B.S. in biochemistry and microbiology. He can be reached at robferguson@ frenchcreeksoftware.com. This technical paper was presented at the 2019 AWT Annual Conference, which was conducted September 11–14, 2019, in Palm Springs, California.
6. Griffiths, D.W.; Roberts, S.D.; Liu, Y.T. (1979). “Inhibition of Calcium Sulfate Dihydrate Crystal Growth by Phosphoric Acids: Influence of Inhibitor Structure and Solution pH,” Society of Petroleum Engineers, International Symposium on Oilfield and Geothermal Chemistry.
37
the Analyst Volume 27 Number 1
What Does Your Warehouse Staff Want
North Metal and Chemical Company provides corrosion inhibition raw materials to solve your boiler and cooling water challenges.
Serving AWT members as the largest and best value manufacturer of Sodium Molybdate in North America! North@NMC-NIC.com | 717.845.8648 See our technical data and SDS documents at www.nmc-nic.com/newsite/products Now stocking both in California and our York, PA manufacturing plant.
Fourth generation, family-owned company since 1921. Most orders ship same or next day! Major credit cards accepted.
in TOTES and DRUMS? BUTTRESS COARSE THREADING for QUICK VACUUM PREVENTION
E CARBOYS and DELL DRUMS for SMALLER NEEDS
NTP BUNG THREADING for PUMPS and VALVES
E CAM-LOCK QUICK DISCONNECT
BALL VALVES for MULTI-USE LEAK PREVENTION
EASY SHIP PAILS with POUR SPOUT
Shipping U.S. Specification drums and totes. We care about the details. Just like you.
How Operating Risks Should Be Managed in Industrial RO Systems Loraine A. Huchler, P.E., MarTech Systems Inc.
40
the Analyst Volume 27 Number 1
Introduction
The objective of this article is to provide options for avoiding or mitigating common risks of operating reverse osmosis (RO) systems installed in industrial facilities. The most common risks in industrial facilities include inadequate pretreatment, poor idling strategies, and improper or insufficient cleaning protocols. This article defines best practices for the design and operation of RO units and includes several case histories that describe the impact of the most common design and operating risks for RO units in industrial facilities.
Discussion Operating and Idling Strategies System owners should strictly limit the flowrate of the RO feed stream to a minimum of 95% of the design specification and consistently control the duration of idling to obtain reliable operation. Idling or operating below 95% of the design flowrate for the feed stream results in several problems, including: Measurably higher fouling rates and increased pressure differentials. Reduced permeate production and increased concentrate flow. Increased frequency of cleaning and shorter membrane life. The most common reason that plant personnel operate RO units below the design flowrate or idle units is because of seasonal or process-related changes in demand for permeate, especially if the plant uses permeate for processes with intermittent demand. When plant personnel idle excess RO units for extended periods of time, they create new risks, which consist of the following: Severe bacteria fouling that may result in irreversible loss of membrane performance. Increased frequency of cleaning that contributes to reduced membrane life.
Managing Risks of Intermittent Operation Installing RO permeate storage tank(s) can eliminate or reduce the frequency of idling. However, it is not always practical to install tanks because of space limitations, capital costs, and the length of periods of increased permeate demand. One solution is to limit the maximum idle-time to four hours to minimize bacteria fouling. Polyamide (PA) RO membranes are very vulnerable to bacteria fouling because these membranes have a very low tolerance for free chlorine. Continuous low concentrations of free chlorine will eventually irreversibly damage the membrane, creating poor quality permeate. RO manufacturers caution end users that exposure of the membranes to greater than 1,000 parts per million (ppm)-hours of free chlorine will result in irreversible damage of the membrane, increasing the salt passage and decreasing the permeate quality. Another solution is to size the RO unit to match the “low season” demand and rent mobile RO assets during peak seasonal demand for permeate. For extended periods of idling, the best option is to remove membranes from the housings after cleaning and to store them in preservative or use an outsourced membrane exchange service to clean and return the same or other cleaned membranes sealed with preservative.
Bacteria Management Strategy Minimizing bacteria fouling ensures the proper flux and reduces the frequency of membrane cleaning. The short-rinse sequences before shutdown and startup are ineffective at removing bacteria that is fouling the membrane surface. For nonpotable applications, DOW (1) endorses the use of a nonoxidizing biocide, DBPNA (2,2-dibromo-3-nitrilopropionamide), to remediate or control bacteria fouling. DBPNA is a very large molecule that cannot pass through an intact membrane; the biocide is rejected into the concentrate. Some plants inject DBPNA into the membrane immediately prior to idling; other plants inject DBPNA continuously or intermittently into all operating RO trains to control the rate of bacteria fouling. Pretreatment Ensuring proper pretreatment is critical to maintaining reliable RO operation; membranes are not tolerant of
41
the Analyst Volume 27 Number 1
How Operating Risks Should Be Managed in Industrial RO Systems continued
suspended solids; improper operation of the upstream clarifier and/or filtration equipment can permanently damage the downstream RO membranes. Overfeed of cationic coagulant in the upstream clarifier and subsequent carry through the filters will make the membranecleaning process difficult or impossible. High rates of anionic flocculant feed will also cause membrane fouling. Silt density index (SDI) is a test developed specifically to evaluate the fouling potential of the water on semi-permeable membranes. It is an imprecise measure of the concentration of suspended solids in water and only generally related to turbidity. Waters with low turbidity (<0.5 Nephelometric Turbidity Units [NTU]) can have high SDI values because the SDI test method allows detection of smaller particles than the turbidity test method. SDI doesn’t exactly match the mechanism of an RO membrane because the SDI test forces all suspended solids through a 0.45-micron (µm) filter; however, it is the best model available. System designers typically specify multimedia filters upstream of the RO to reduce the SDI. Other tactics to reduce SDI include the feed of coagulant chemicals or the installation of ultrafiltration (UF) equipment upstream of the RO. UF is a membrane-based technology that has a much greater efficiency than media filters in removing suspended particles. Most UF membranes are compatible with free chlorine, allowing operators to inject bleach into the backwash procedure to reduce the risk of bacteria proliferation in the UF unit. Data obtained from an SDI test has several uses: Designing a new RO system. Evaluating a change in the feedwater quality. Measuring the effectiveness of the pretreatment equipment or chemical additives. Clarifiers that serve RO systems must produce water with a low SDI (< 5). Inorganic coagulants, especially the ferric salts, seem to be very effective at reducing SDI. Dechlorination. For PA membranes, operators must remove all chlorine-containing compounds from the feedwater to prevent destruction of the RO membranes. 42
There are two methods for removing chlorine: an activated carbon filter or sodium bisulfite injection. Activated carbon filters require a high level of maintenance to avoid premature exhaustion and the addition of biological material and carbon fines to the RO feedwater. The sodium bisulfite feed is highly preferred for most industrial RO systems. Some operators feed alternate forms of sulfite. As shown in Table A, the recommended dosage for dechlorination is two times the stoichiometric concentration. Chemical suppliers typically blend sulfite with a cobalt catalyst for use in boiler feedwater systems. The catalyst improves the speed of the reaction of sulfite with dissolved oxygen but has no effect on the reaction rate of sulfite with chlorine. RO experts recommend the uncatalyzed forms of sulfite chemicals because the cobalt could catalyze oxidation of metal contaminants on the membranes, causing permanent degradation. Table A: Dechlorination Stoichiometry Stoichiometric Concentration (ppm chemical per ppm free chlorine)
Stoichiometric Dosage (ppm chemical per ppm free chlorine)
Sodium sulfite (Na2SO4)
1.77
3.54
Sodium bisulfite (NaHSO4)
1.46
2.92
Metabisulfite (Na2S2O5)
0.70
1.40
Chemical
Prefilter design. A prefilter serves as a secondary defense against particulates reaching the membranes; it does not substitute for robust upstream media filters or UF units, nor does it protect against catastrophic failure of upstream filters or clarifiers. Careful monitoring of the pressure differential across the pre-filter unit and prompt replacement of filter elements is essential to managing the reliability of the downstream membranes. These prefilters are often a source of risk because routine replacement of elements is a time-consuming maintenance activity, and the elements are rather expensive. There is a risk of maintenance substituting larger-micron filter elements to reduce the frequency of changeouts for plants that have difficulty controlling the concentration of suspended solids in the RO feed stream. The force of the RO feed stream can be high enough to lift the Analyst Volume 27 Number 1
How Operating Risks Should Be Managed in Industrial RO Systems continued
filter elements from their seats, bypassing the prefilter and risking catastrophic damage in the downstream RO elements when suspended solids carry through the upstream media filters.
Chemical Treatment All oxidizers will degrade PA membranes, including all forms of chlorine, ozone, peroxide, bromine, and peracetic acid. Chlorine dioxide typically has low but measurable concentrations of free chlorine, creating a similar risk for treatment of PA feed streams. Chloramines, although extremely stable, will also damage the membrane. PA membranes can tolerate a maximum of 300,000 ppm-hours of exposure to chloramines under the following conditions: ƒ Chloramines are formed from adding chlorine to waters with naturally occurring ammonia.
Operators should not expect antiscalant chemicals to prevent scaling for water that does not meet the specification limits shown in Table B. The feed of antiscalant chemicals is designed to accommodate the dynamic inefficiency of the upstream pretreatment equipment and variability in the quality of the feedwater. Table B: RO Membrane Feedwater Quality Requirements Contaminant
Parameter
Typical Limits
Suspended solids
SDI turbidity
<5 (preferably <3) <0.5 NTU
Organics
TOC
<3 ppm
Color
Color
<3 APHA
Metals
Total iron, manganese, barium, strontium
<0.05 ppm
Dissolved solids
Concentrate LSI without antiscalant
<0 <2.5 50–160 ppm
Concentrate LSI with antiscalant Concentrate reactive silica
ƒ There is no detectable free chlorine residual.
Hydrogen sulfide
From a practical perspective, it is difficult to meet these two conditions because adding chlorine compounds to waters with naturally occurring ammonia creates a dynamic equilibrium between free chlorine and ammonia, usually resulting in unacceptably high concentrations of free chlorine. Many plants feed antiscalant chemicals to the feed stream to reduce scaling and increase the interval between membrane cleanings. There are a variety of antiscalant chemicals available, including mineral acids, sequesterants (e.g., phosphonates, chelants), dispersants, and proprietary formulations that are matched to specific scaling agents, such as hardness or silica. Sulfuric acid is often fed at the RO inlet to reduce the Langelier Saturation Index (LSI) below 1.0 and minimize scaling. Hydrochloric acid is preferred if the inlet water has a high concentration of calcium, risking the formation of insoluble calcium sulfate. Operators should never mix these treatment chemicals together in the same day tank or feed point. Nor should the day tank solution be kept for more than three days because there is a risk of growth of microbiological organisms, hydrolysis of organic phosphates, and precipitation of active chemicals.
43
Hydrogen sulfide
<0.1 ppm
If the RO concentrate is reused in another process unit, remember that membranes reject more than 99% of the antiscalant chemicals into the concentrate. The presence of these antiscalant chemicals may negatively impact the unit receiving the concentrate.
Membrane Cleaning Strategies Cleaning removes scale from precipitation of inorganic contaminants and foulants from microbiological organisms and suspended solid contaminants. Minerals (inorganic soluble contaminants) concentrate on the surface of the membrane, forming nucleation sites for additional scale and foulants. Excessively high mineral concentrations will cause scaling on the membrane surface. The concentration of minerals is highest in the last element in the tube. If the unit has two stages, the concentration of minerals is highest at the last element of the second stage. Similarly, for a three-stage RO, the highest risk of scaling occurs at the last element in the third stage. Organic contaminants, suspended solids, and bacteria are known as foulants. Typically, foulants accumulate on the first element of each tube. If the unit has several stages, the first stage will have the most severe fouling problem. All RO systems that use surface water or reused water as the inlet water are vulnerable to microbiological the Analyst Volume 27 Number 1
How Operating Risks Should Be Managed in Industrial RO Systems continued
growth (MB) and require an intensive MB control program and frequent membrane cleaning. Other sources of MB include well water that may have anaerobic bacteria, and poorly maintained chemical feed systems. If your RO membrane has a bad odor or if the inside of the housing has a layer of slime, you can be certain that you have a bacteria (MB) problem. It’s highly likely that bacteria have fouled the cartridge prefilter and may have fouled the upstream deep-bed filters. Corrective actions include replacing the cartridge elements in the prefilter, sampling the top inch or two of media in the upstream deep-bed filters to check for bacteria, and cleaning or replacing the filter media if it is fouled. The optimal timing for an offline cleaning occurs when the normalized performance declines by a predetermined percentage. The ideal cleaning interval is typically three months; however, RO systems that use surface water and have inadequate pretreatment may require cleaning as frequently as every three weeks. Soluble iron and manganese in the feed can oxidize and deposit as a foulant onto the membrane and can catalyze oxidation of the membrane, causing permanent damage. If hydrogen sulfide is present in well water that feeds an RO, it can oxidize to form a sticky, adherent colloidal sulfur foulant. Operators should rearrange the flow path and clean each RO stage separately to avoid moving foulants from membranes in one stage onto membranes in another stage.
Selecting Cleaning Chemicals Engineers and operators should design the offline cleaning procedures to match the foulant or scale on the membranes. Precise determination of the foulant or scaling agent requires destruction of a membrane or “autopsy,” a time-consuming and expensive procedure. A membrane autopsy is appropriate if previous efforts to design the correct cleaning protocol have been unsuccessful. Most operators analyze the quality of feedwater and compare it to the typical specifications in Table B to initially select cleaning chemicals. Known excursions in the quality of the feedwater or an understanding of the weaknesses of the pretreatment system provide important data to select the optimal cleaning chemicals. 44
For example, if the multiport valves on the upstream sodium zeolite softeners have seal problems, the RO inlet stream would have highly variable concentrations of hardness—and the cleaning procedure should include a step to remove the inorganic calcium scale. RO experts disagree about cleaning protocols, and specific experience from previous cleanings is also helpful. Sampling and visually or chemically analyzing the spent cleaning solution can provide additional information about the effectiveness of the cleaning procedure (Table C). Operators should document their observations during cleaning for use in subsequent cleaning processes. Table C: Observations of Spent RO Cleaning Solution Observation
Possible Causes
Brownish color
TOC; color of spent Organics, lignins, tannins from surface cleaning solution remains after water adding acid Iron
Test
Clear
Hardness (calcium carbonate)
Colorimetric or spectrophotometric iron test; spent cleaning solution becomes clear after adding acid
Table D provides additional information about selecting the correct cleaning chemicals based on identifying the operating problems. Table D: RO Cleaning Recommendations Contaminant
Type and pH of Cleaning Chemicals
Organics Sulfates
Surfactants, sequesterants High pH (11–12.5)
Micro-organisms
Biocides Neutral pH (6–7.5)
Inorganic Scale Carbonates
Chelants, acids Low pH (2–3.5)
Monitoring Most industrial RO systems have online data acquisition systems that collect and trend data and sound alarms for off-spec conditions of online parameters. Normalized data. The reason for normalized data is to adjust for the large differences in water density as a function of temperature. RO flow volume increases by approximately 1.8% per degree Fahrenheit (°F) (3.3%/°C the Analyst Volume 27 Number 1
How Operating Risks Should Be Managed in Industrial RO Systems continued
increase) in temperature at constant feed pressure and feed quality. To accurately detect changes in key parameters, operators must adjust the value of each data point to account for the effect of temperature on water density. The volume of product water from RO membranes increases as the water temperature increases due to the change in water density. The flux or volume of product water per unit area increases as the feed pressure increases due to an increase in the driving force of water through the membrane. The volume of reject also increases. Fouling, scaling, and membrane degradation decrease the volume of permeate from RO membranes. This adjustment calculation is called normalization. Failing to adjust or “normalize” the data to account for the effects of temperature, pressure, and concentration can lead to false conclusions about the system performance. The three most important transport properties for membrane designers when evaluating membrane performance are: 1. Water flux, which is the flowrate of pure water through the membrane per unit area of the membrane surface. 2. Salt flux, which is the flowrate of dissolved contaminants through the membrane per unit area of the membrane surface. 3. Differential pressure, which is the difference between the feed pressure and the concentrate pressure. The calculations for normalized water flux and salt flux are so complex that RO membrane manufacturers provide software programs to automatically calculate normalized water and salt flux. The software requires initial design operating parameters and current temperatures, pressures, and flowrates. For accurate normalized flux results, the initial design or standard operating parameters must be correct! Data management. Proper data management supports troubleshooting efforts, performance-based cleaning, and membrane replacement events, maximizing system performance and minimizing operating costs. The 45
volume of data required to manage an RO system is so great that the only reasonable method is to ensure that the online analyzers automatically route data to a historian. Baseline membrane performance. One of the most important tasks following commissioning of new membranes is to document the performance. Review the trend data for the normalized parameters following installation of new membranes and select the subset of data during the first two weeks of operation that show steady state values for these three metrics: water flux, salt flux, and differential pressure. The purpose of documenting the baseline performance metrics is to track the health of the membranes. As the membranes accrue time in service, they will typically become fouled and/or damaged. The comparison between the current operating metrics and the baseline performance metrics provides a quantitative measure of the degradation of the membrane’s performance.
Membrane Replacement The optimal strategy for membrane replacement uses membrane performance as the primary metric to schedule replacement of all membranes. Triage for failing membranes. Operators can extend the life of failing membranes by a few weeks by employing one or both of these strategies: Discard the first element in each housing and install a new element in the first or last position; the first element is the most heavily fouled element. Flush the unit prior to returning it to service. Remove and rotate each element 180° and reinstall the brine seals properly, effectively “switching” the feed and concentrate sides. Flush the unit prior to returning it to service. Membrane manufacturers offer high-capacity membranes that operate at higher flowrates, increasing the volume of product flow for the same feed pressure as standard membranes. Beware of these high-capacity modules; they have smaller spacers between the membrane layers, making them more vulnerable to fouling. These membranes should not be used in systems with surface water unless the pretreatment system the Analyst Volume 27 Number 1
How Operating Risks Should Be Managed in Industrial RO Systems continued
Divert the RO concentrate to the publicly owned treatment work (POTW) drain instead of recycling the stream to the warm water system to conform to the U.S. Department of Agriculture (USDA) regulatory requirements for water used for cleaning equipment.
has a UF unit and operates with a very high degree of reliability.
Case Histories
The following six case histories illustrate the most common problems for industrial RO systems.
Case #2
Case #1
Situation: Dual train; two-stage oversized RO units; potable feed; long idle time; and concentrate recycle.
A Midwestern beef processing plant uses RO permeate as makeup to their gas-fired Kemko steam generators for direct-contact heating of water used for sterilization of processing equipment. The plant intermittently sequences each of the two RO trains (150 gallons per minute/train [gpm/train]) to meet the recently reduced permeate demand of 56 gpm. The permeate storage tank has a small dead band and no permeate recirculation, resulting in very short intervals of operation of one RO train (<10-minute cycle) while the other RO train is idle. The plant does not conduct onsite membrane cleanings; the typical interval for membrane exchange with their supplier is one year due to bacteria fouling of the membranes. To reduce the cost of potable water, the plant recycled the RO concentrate into the warm water system. Lesson Learned Oversized RO units will operate at very short duty
cycles, increasing the volume of flush water and decreasing the mechanical reliability of the solenoid valves. Long idling periods for the RO membranes increases the rate of bacteria fouling, reducing the permeate production rate. The warm-water system contains hydrocarbon combustion products from the Kemko steam generator that serve as nutrients for bacteria introduced by the recycled concentrate stream.
Best practices Reconfigure the RO unit to more accurately match the
system capacity to the permeate demand. Maximize the dead band on the downstream RO storage tank to ensure sufficiently long RO operating cycles and implement an idling procedure to ensure that each RO train is idle for a period not longer than four hours.
Return the excess RO membranes to the vendor for
cleaning and credit for future membrane exchanges. 48
Situation: Dual-train, two-stage oversized RO units; potable feed; long idle time; and discharge of permeate directly into a pressurized transfer pipe.
A sugar refinery in the northeastern United States installed an RO unit that discharged permeate directly into a transfer pipe that joined with condensate prior to entering the deaerator. The logic for the process control system gave condensate first-priority to feed the deaerator, back-pressuring the permeate stream and forcing the RO unit to operate at a low-duty cycle and variable flowrates. Since RO units dramatically lose efficiency at flowrates below 95% of the design specification, the membrane fouling and the pressure differential increased and the permeate production rate and quality decreased, forcing more frequent cleanings and a reduction in the service life of the membranes. Lesson Learned The installation of a permeate storage tank and the
associated transfer pump to supply permeate to the deaerator would optimize the RO operation, minimizing the rate of fouling and maximizing product quality and membrane service life.
Best practice Always configure the permeate piping to discharge to
atmospheric pressure by installing a permeate storage tank and the associated transfer pump. Analyze the typical minimum and maximum permeate demand and size this tank to accommodate the dynamic demand profile. For periods of very low permeate demand, the installation of permeate recirculation would increase the duty cycle on the RO units, reduce the length of the idle periods, and reduce bacteria fouling of the membranes.
Case #3
Situation: Dual-train, two-stage RO units; cold-limesoftened, media-filtered and softened feed; improper idling of RO trains; poor monitoring; and ineffective risk assessment and management.
the Analyst Volume 27 Number 1
How Operating Risks Should Be Managed in Industrial RO Systems continued
A refinery that upgrades tar sands in Alberta, Canada, has several RO trains served by an upstream cold lime softener, multimedia filters (MMF), and cartridge filters. All the chemical feed control for the cold-lime softener system are manual, including the flocculant feed control. The RO feed pumps were automatically shutting down due to low suction pressure caused by carryover from the lime-softening unit and overfeed of flocculant that plugged the MMF units and the cartridge filters. The carryover was severe; operators were replacing the disposable filter cartridges every two weeks. Although plant personnel flushed idled RO trains every 12 hours, autopsy results of a 3-month-old membrane indicated severe bacteria fouling. Lesson Learned Feed control for lime softening chemicals is critical
for systems with downstream RO units; the carryover of lime solids and overfeed of flocculant caused channeling of the multimedia filters and breakthrough of solids in the cartridge filters that contaminated the membranes with suspended solids, bacteria, and associated micro-nutrients. Flushing idled RO trains is not sufficient to reduce the risk of bacteria fouling; operators must sequentially operate and idle RO trains every four hours to control the risk of bacteria fouling.
Best practice Improve the operating discipline and chemical feed
strategy for the cold lime softener to reduce carryover, channeling in the multimedia filters and solids breakthrough in the cartridge filters. Install an online turbidity analyzer at the cold-lime softener outlet with remote readout and alarms to provide an early warning of the risk of carryover. Instead of flushing membranes, sequentially cycle into service each idled RO train every four hours to reduce the risk of bacteria colonizing the membrane surfaces.
Case #4
Situation: Three trains; two-stage RO units, cold-limesoftened, and media-filtered feed; improper monitoring; data management and corrective actions.
A coal-fired electric power plant in the western United States has three RO systems that produce a total of 300 gpm of permeate. The feedwater is cold-lime-softened, media-filtered water heated to a temperature between 55 °F and 65 °F. Operators were cleaning membranes on 49
a fixed schedule and were not monitoring normalized parameters because they concluded that the 10 °F variability in the feedwater temperature was not significant. Lesson Learned Although the temperature range for the RO feedwater
was 10 °F, the permeate flowrate decreases by 1.8% for every 1 °F reduction in temperature—or an 18% reduction in permeate flowrate when the RO feedwater decreases from 60 °F to 50 °F. Without normalized data, operators were not able to accurately identify the proper time to clean the membranes and prevent a permanent loss of permeate flowrate or quality.
Best practice Monitoring membrane health requires tracking
normalized parameters (e.g., product flowrate, salt passage, pressure differential) and implementing corrective action to optimize the performance and service life of membranes.
Case #5
Situation: Five trains of two-stage RO units; cold-limesoftened, ultrafiltered and softened feed; improper idling of RO trains; poor monitoring; and ineffective risk assessment and risk management.
A large, integrated Texas refinery has an RO system downstream of a cold-lime softener and an UF unit. Despite excellent operation of the pretreatment systems, the membranes had high rates of bacterial growth. Operators were cleaning the membranes once per week to maintain permeate production rates. Operators did not monitor normalized data; they were incorrectly assuming that the membrane performance was satisfactory because the permeate quality consistently met the plant’s rather-high specification limit for the concentration of silica in the permeate. Ultimately, the damage from too-frequent cleaning resulted in off-spec permeate quality and premature replacement of membranes, increasing operating costs. Lesson Learned Too-frequent membrane cleaning requires imme-
diate corrective action to ensure system reliability and performance. Monitoring membrane health requires tracking normalized parameters (product flowrate, salt passage, pressure differential) and implementing corrective action to optimize the
the Analyst Volume 27 Number 1
How Operating Risks Should Be Managed in Industrial RO Systems continued
service life of membranes. Strict bacteria control is critical to minimize the number of cleanings, ensure permeate quality, and maximize the service life of the membrane. Best practice OEM suppliers of membranes recommend a maximum
of four cleaning procedures per year to ensure the standard service life of three years. Operators should empirically determine a feedrate and feed strategy for the nonoxidizing biocide, DBPNA, during service and idling to reduce bacteria growth and reduce the frequency of cleaning and the negative impact on the performance and service life of the membranes.
Case #6
Situation: Six trains of two-stage RO units; cold-limesoftened, media-filtered and softened feed; improper idling of RO trains; poor monitoring; and ineffective risk assessment and risk management.
A large, integrated petroleum refinery in the Midwest installed an RO system with a capacity of 5,000 gpm of permeate with the mistaken belief that they could abandon their sodium-zeolite softeners. The aging pretreatment system (cold-lime softener, anthracite filters, and sodium-zeolite softeners) produced RO feedwater with an SDI measurement consistently above 5, despite high feed rates of antiscalant chemicals. For several months, the aging upstream sodium zeolite softeners had been sending “shots” of brine and leaking hardness into the RO feed stream because of the plant’s failure to maintain the multi-port valves in good working order. The high hardness in the RO feed began to scale the RO membranes, reducing the permeate flowrate and resulting in high concentrations of hardness in the permeate and scale deposits in the downstream fired and waste heat boilers. The lack of risk management included a failure to conform to plant standards for stainless steel materials for all chemical feed transfer piping. One day, the plastic transfer tubing for the coagulant feed to the upstream cold-lime softener failed, resulting in extremely high-turbidity water delivered to the upstream anthracite filters and softeners. The force of the suspended cold-lime solids damaged the underdrains of the anthracite filters and softeners, sending cold-lime 50
solids and zeolite resin into the RO prefilter. The force of this “slurry” exceeded the tension on the stainless streel springs holding the pre-filter elements in place, allowing cold-lime solids and zeolite resin to bypass the prefilter elements, causing irreversible damage to the membranes—with a force that sheared the membrane inter-connectors. Lesson Learned
Plant personnel failed to assess and manage the risks of pretreatment systems: they improperly integrated the RO unit into the existing pretreatment system and failed to properly operate, diagnose, troubleshoot, maintain, and manage the cold-lime softener, anthracite filter, and softener assets. A risk assessment would have identified the design
noncompliance and the high risk of failure of the plastic tubing on the discharge of the coagulant feed pump as well as the negative consequences of this “local control” feed pump in a remote part of the plant. In the absence of this catastrophic failure, there was still a high risk of poor performance of the RO unit and risks to the integrity of the downstream steam generators because plant personnel failed to properly design the pretreatment system to meet the requirements for RO units (SDI <5) and implement an appropriate level of operating discipline for the existing pretreatment assets.
Best practice Conduct a risk assessment of the entire pretreatment
system and make changes to equipment configuration, and monitoring and operating practices to reduce the risks. Use rigid piping for the discharge of chemical feed pumps, install remote verification and alarms on the coagulant feed pump for the cold-lime softener that serves the RO system, and provide either an installed or on-the-shelf spare coagulant feed pump. Educate your operations staff and implement a strict operating discipline to ensure early warning of off-spec conditions.
the Analyst Volume 27 Number 1
How Operating Risks Should Be Managed in Industrial RO Systems continued
Reference 1. DOW Chemical (n.d.). “Water Chemistry and Pretreatment: Biofouling Prevention of FILMTEC Elements with DBNPA,” technical brochure, Midland, MI.
Bibliography Bersillon, J.; Thompson, M. (2003). Water Treatment Membrane Processes, McGraw-Hill, New York, NY.
Byrne, W. (1995). Reverse Osmosis: A Practical Guide for Industrial Users. Tall Oaks Publishing Inc., Littleton, CO. Huchler, L. (2007). Operating Practices for Industrial Water Management, Influent Water Systems, pp. 177–221, Gulf Publishing Co., Houston, TX.
Kucera, J. (2010). Reverse Osmosis Industrial Applications and Processes, Wiley, Scrivener Publishing, Hoboken, NJ.
Loraine Huchler is the founder and president of MarTech Systems Inc., an engineering and consulting organization. Ms. Huchler recently concluded more than 15 years as author of a quarterly column, “HPIn Water Management,” for an international trade journal, Hydrocarbon Processing, and has published her first of a series of four books: Operating Practices for Industrial Water Management. She has a bachelor of science degree in chemical engineering from the University of Rochester. Ms. Huchler belongs to several technical societies, including AIChE and NACE, and has served three terms as the president of the New Jersey section of the Society of Women Engineers. She can be reached at huchler@martechsystems.com. This paper was originally presented at the International Water Conference, which was conducted on November 4–8, 2018, in Scottsdale, Arizona. More information is available at www.eswp.com/water.
51
the Analyst Volume 27 Number 1
Part 5: An Overview of IX Resins for Water Treatment Peter Meyers, ResinTech Inc.
52
the Analyst Volume 27 Number 1
Preface
“An Overview of Ion Exchange Resins” is Part 5 of a series of articles that have covered various aspects of how ion exchange (IX) resins are used. Not the actual applications, but the physical aspects of touching resins, feeling them, and caring for them. This part brings together the information shared in Parts 1 through 4 and covers general resin use, including what resins are, safety aspects related to resins, materials compatible with resin, contamination of resin, and documentation associated with their use. If you are charged with the responsibility for storing, moving, loading, unloading, or disposing of IX resins and have not done it before, it may be worth hiring someone knowledgeable to guide you through it the first time.
Introduction
IX resins are quite commonly used as a process step in the treatment of boiler water, cooling water, ultrapure water, and wastewater. Resin storage requirements are sometimes discussed briefly in resin manufacturers’ literature, but detailed discussions about best practices for replacing IX media are sometimes overlooked, and requirements for safe disposal are often ignored entirely. Nonetheless, IX resins do wear out and must be replaced at irregular intervals. Therefore, users of IX resins should be prepared to deal with the ins and outs of unloading, reloading, storage, and disposal of IX resins. In this series, we have discussed basic information about IX resins; the detailed requirements for storage; moving IX resins from place to place; and loading, unloading, and disposal. This information is intended to be a reference guide, irrespective of the type of equipment or the manufacture of the IX resin itself.
What Are Ion Exchange Resins?
A simple explanation of IX resins is that they are “plastic beads that take salts out of water and put other salts back in.” Physically, IX resins are solid plastic spheres approximately 0.6 millimeter (mm) in diameter with specific gravity somewhat greater than water. There are several different plastics that can be used, but the vast majority of IX resins are made from polystyrene polymer, the remainder almost all from acrylic polymer. The beads are “functionalized” with various acids and bases that give them their IX properties. Thus, IX resins can also be described as solid acids and bases. A fixed charge is permanently attached to the plastic, while a mobile “counter-ion” is free to exchange in and out of the beads. The fixed charge can be either sulfuric acid (in the case of strong-acid cation resin), carboxylic acid (in the case of weak acid cation resin), or various amines (in the case of anion and chelating resins). The counter-ion can be almost anything that is ionized; various salts, acids and bases; radioactive contaminants; hazardous metals; poisons; precious metals; pharmaceutical chemicals and drugs; and so on. The counter ions, rather than the fixed charges, often dictate how resin needs to be stored, handled, and disposed of. Figures 1 and 2 show examples of industrial IX systems. Figure 1: An aging demineralizer system still in use in southern Florida. Would you look this good if you stood outside in the Florida sun and rain for 50 straight years?
“A simple explanation of IX resins is that they are ‘plastic beads that take salts out of water and put other salts back.’”
53
the Analyst Volume 27 Number 1
Part 5: An Overview of IX Resins for Water Treatment continued
“Gloves and safety glasses are
Figure 2: One of several chromate-removal systems in use at the Hanford site in Richland, Washington. These systems have been in use indoors for 10 years now and still look like they were installed yesterday.
recommended when handling any IX resin.” wear additional protective gear, as IX resins, in and by themselves, are not considered hazardous. However, even salt forms of IX resin can cause rashes with prolonged exposure to sensitive skin.
Safety Aspects When Handling IX Resins
Spilled resin always represents a slipping hazard. The beads are like tiny ball bearings and make smooth surfaces quite slippery. Even nonhazardous spills should be swept up promptly to prevent possible injury to unsuspecting passersby. Resin beads are small enough to be an eye hazard. Even neutral salt forms of resin sting like crazy if they get in your eye. The hydrogen and hydroxide forms can be quite dangerous due to their acidic or basic properties and can cause permanent eye damage. Hydrogen and hydroxide forms of IX resins can be significantly acidic or alkaline. If it could actually be measured, the internal pH of a hydrogen-form strong-acid cation resin would be close to 0, while the pH of a hydroxide-form strong-base anion resin would be close to 14. It can’t be measured because the acid or base is inside the solid plastic. The acidity (or causticity) is activated by moisture. Touching hydrogen or hydroxide-form resin beads with dry hands does not cause an immediate chemical burn, but prolonged exposure, especially in a humid or wet environment, will cause burns. Chemical burns look and feel just like thermal burns. Burns from acid (especially sulfuric acid) occur rapidly, but burns from caustic can cause longer lasting damage and are more difficult to treat. Gloves and safety glasses are recommended when handling any IX resin. In general, it is not necessary to 54
Although there is little danger of ingesting the beads, certain resins, notably hydroxide-form anion resins, can cause considerable stomach distress if swallowed. Hydroxide-form anion resins have a strong fishy odor (from the amines). Good ventilation is recommended when opening containers of hydroxide-form anion resins. In cases where hydroxide-form anion resins must be exposed in a confined space, respirators with filters suitable for ammonia and amines should be worn. A few other types of IX resins may have a sulfide or rotten egg odor, or an ammoniacal odor. Hydrogen- and hydroxide-form IX resins are strong enough acids and bases to cause chemical burns following prolonged skin contact and can cause permanent eye damage. When hydrogen- and/or hydroxide-form IX resins must be directly handled, goggles and long sleeve shirts are recommended, in addition to gloves. Resins that have been used to remove hazardous substances take on some of those hazardous properties. Additional personal protective equipment (PPE) is then needed, according to the nature of those hazardous substances.
Uses of IX Resins
IX resins are used for a myriad of water treatment applications: for residential softening to protect piping systems and water heaters from scale, in the manufacture of pharmaceutical chemicals, for removal of radioactive contaminants, as catalysts, in the manufacture of semiconductors and other high-tech devices, and for thousands of other uses. IX resins are at their best removing a thimble’s worth of contaminant from a sea of ordinary salts. They are capable of separations not possible by any other means. Not a day goes by in our modern lives that isn’t enhanced by products that depend on IX resins as part of their manufacturing process. the Analyst Volume 27 Number 1
Part 5: An Overview of IX Resins for Water Treatment continued
Limitations of Use for IX Resins
IX resins are generally quite robust. They can withstand temperatures up to about the boiling point of water, static pressures of thousands of atmospheres, and contact with most solvents and salts. Most limitations are pragmatic rather than destructive. The list in Table A, although not exhaustive, covers most of the more common limitations. Table A: IX Resin Types and Their Limitations Resin Type
TDS Limit (ppm)*
Strong cation resin (Na form)
1,000
Strong cation resin (H form)
500
Strong anion resin (Cl form)
1,000
Strong anion resin (OH form)
500
Weak cation resin (Na form)
10,000
Weak anion resin (acid/salt form)
10,000
Chelating cation resin (Na form)
No limit
Mixed-bed resin
500
5. 6.
ii. Some polymers react with IX resins pH— Stable from pH below 0 to above 14 Temperature—Salt forms stable to at least 140 °F i. Salt-form resins generally more stable than the hydrogen (H) or hydroxide (OH) forms ii. Acrylic strong-base anion resins are more sensitive than other types iii. Elevated temperatures decrease IX selectivity and increase leakage iv. Temperatures close to the freezing point of water dramatically slow the IX rate
Regeneration and Reuse of IX Resins
*Note that the TDS limits shown are pragmatic and not absolutes—exceptions exist.
The following list summarizes the sensitivity of IX resins to inlet contaminants: 1. Chlorine (and other oxidants)—Poor i. Chlorine levels less than 0.3 milligrams per liter (mg/L) usually do minimal damage ii. Oxidation releases toxic leachables iii. Hydrogen-form cation resins are particularly sensitive (1) Leachables from hydrogen-form cation resins are known to foul anion resins 2. Suspended solids— Poor i. One Nephelometric Turbidity Unit (NTU) or less generally safe ii. IX resins filter to approximately 2-micron (µm) nominal iii. IX resins are coalescing medias and cause particles to agglomerate 3. Polar and nonpolar solvents—No consequence? i. IX resins may swell or shrink ii. Internal water can be replaced with the solvent, dehydrating the resin and diluting the solvent iii. Resins must be dried for use with solvents that are not miscible with water 4. Polymers and other long chain molecules Poor i. Anything that coats the surface interferes with IX 55
For the most part, IX resins can be regenerated and reused for thousands of cycles. Regeneration is the process where the resin is restored to a desirable ionic form by passing a solution containing the desired ion through the resin. The resin exchanges the ions it picked up during the exhaustion cycle for the desired ion, thus replenishing the resin and preparing it for the next exhaustion cycle. Although it is impossible to list every chemical possibility, the most common regenerants include strong acids such as sulfuric acid and hydrochloric acid, strong bases such as sodium hydroxide, and common salts such as sodium chloride. It should be understood that molecular liquids such as sugar solutions, amines, glycols, and others are not ionized and therefore do not exchange with IX resins. These solutions can in many cases be purified by IX resins that remove the ions contaminating the molecular solutions. However, molecular liquids that are not water soluble cannot penetrate the beads unless the beads are dried. Therefore, applications such as acid neutralization of oils and hydraulic fluids requires that the resin be pre-dried. Alcohols, glycols, amines, and other water-soluble liquids that are close to anhydrous dehydrate the resin and dilute the liquid. Although dehydration usually does not damage resin beads, rehydrating them requires special procedures to avoid shattering the beads. A few ions have such high affinity for IX resins that they cannot be removed in any practical fashion. These ionic contaminants slowly poison the resin and sometimes limit the resin to single use applications where the spent resin is disposed of rather than regenerated and reused. Examples of high-affinity ions include radium, perchlorate, per- and polyfluoroalkyl substances (PFAS), and alkyl sulfonates. the Analyst Volume 27 Number 1
Part 5: An Overview of IX Resins for Water Treatment continued
Fouling
There are three basic types of fouling that need to be considered, which can somewhat whimsically be described as: 1. The plastic bag 2. The sponge 3. The roach motel The plastic bag refers to substances that coat the surface of the resin beads and interfere with or completely block ions in the liquid from interacting with the resin. Oil is perhaps the best known foulant of this type, but polymers, organic coagulants, scale inhibitors, and any other substances that coat the beads also create a “plastic bag” effect. Ions might still be exchanged, but the resin’s IX behavior will be abnormal. The sponge sucks up ions and contaminants (especially from the regenerant solutions) and later releases them. Sponges also block the void spaces among the resin beads and interfere with the even flow of water through the resin bed. Examples of “sponges” include suspended solids—and iron or other contaminants that precipitate in the resin—and organic bio-growths. In the roach motel, “bugs check in but they don’t check out.” This type of fouling refers to ions that have such
high selectivity for the IX sites that it is difficult or impossible to remove them from the resin. This is not necessarily a bad thing, as certain trace contaminants, such as perchlorate, PFAS, radium, and others, can be removed, and once the resin is exhausted, it can be disposed of. However, for resins that are intended to be regenerated and reused over and over, contaminants with extremely high selectivity for the resin gradually poison the resin and reduce both its capacity and effectiveness. Examples of “roach motel” type contaminants include citric acid, alkyl sulfonates (soaps), aluminum, and barium, among others.
Materials of Construction Compatible With IX Resins
By and large, plastic or stainless steel materials are best for contact with IX resins. Although, iron, steel, and aluminum can be used for salt-form resins (such as sodium-form cation resin and chloride-form anion resin), wet resins are somewhat corrosive and it is better to be safe rather than sorry. When it comes to hydrogen-form cation resin and hydroxide-form anion resins, moisture activates their acidic or basic properties. These forms of resin are more corrosive than the neutral salt forms. Table B summarizes the suitability of various materials that sometimes come in contact with IX resins.
Table B: Suitability of Materials With IX Resins Resin Type Ionic form
Cation Sodium
Anion Chloride
Cation Hydrogen
Anion Hydroxide
PVC
Excellent
Excellent
Excellent
Excellent
Rubber
Excellent
Excellent
Excellent
Excellent
Polystyrene
Excellent
Excellent
Excellent
Excellent
ABS
Excellent
Excellent
Good
Good
Plexiglass
Excellent
Excellent
Good
Fair
Teflon/Kynar
Excellent
Excellent
Excellent
Excellent
Nylon
Good
Good
Bad
Fair
Polyethylene
Excellent
Excellent
Excellent
Excellent
Polypropylene
Excellent
Excellent
Excellent
Excellent
Stainless Steel
Excellent
Excellent
Excellent
Excellent
Steel/Iron
Good
Good
Poor
Fair
Aluminum
Fair
Fair
Poor
Bad
Galvanized metal
Poor
Poor
Bad
Bad
Brass/Copper
Good
Good
Fair
Poor
Explanation of Terms Used in Table B: Excellent: No worries about either corrosion or resin contamination. Good: Little worry about corrosion or contamination except for long-term contact (months or years). Fair: Some corrosion and consequent contamination of resin expected, but may be OK for short duration (minutes or hours) such as loading and unloading. Poor: Avoid even short-term use if at all possible. Do not use for long-term contact due to significant corrosion and consequent contamination of the resin. Bad: Rapid corrosion and consequent contamination of the resin. Not suitable even for short duration use.
56
the Analyst Volume 27 Number 1
Lovibond® Water Testing
Don’t Risk It - Test It! Ask about our innovative solutions for Legionella detection and prevention.
Want To Try Before You Buy? Scan the code & fill out the form. We’ll send you our Legionella Detection Test or Dipslides for FREE!
www.lovibond.com
Need More Information? Contact us For Details: Phone: 941.756.6410
Email: sales@tintometer.us
Offer valid for U.S. Customers Only. Limit of One Per Company. Offer expires February 29, 2020
Part 5: An Overview of IX Resins for Water Treatment continued
For mixed-bed resins, follow the advice for hydrogenand hydroxide-form resins. For weak-acid cation and chelating resins, follow the advice for cation resins. For weakly basic resins, follow the advice for anion resins. For miscellaneous specialty resins, follow the more stringent requirements or seek advice from the manufacturer.
Resin Contamination
Resins can be contaminated by contact with the devices used to move them, by water, and even by direct contact by workers. For the most part, salt-form resins (sodium-form cation resin and chloride-form anion resin) are less susceptible than their acid/base forms (hydrogen-form cation resin and hydroxide-form anion resin). Resins used in the salt forms for industrial applications can be directly handled and loaded with any water that is reasonably clean and free of contaminants such as suspended solids, algae, high levels of organics, and oils, among others. Tanks, piping, and any devices used to move the resin should be rinsed clean before use. Avoid leaving containers of resin open to air except when being actively moved. Remove any foreign debris from the resin before loading into a tank. Resins used for drinking water applications require some additional attention to protect from contamination, especially with the water used to move them. Water used must be potable water to start with, free from harmful bacteria and inorganic contaminants above the maximum contaminant level (MCL).* It is understood that even if a resin is sterile while in its shipping container, as soon as the container is opened, it is exposed and vulnerable, so no longer sterile. Applications that require sterility will require sterilization of the resin, tanks, and piping after the initial loading is completed. *MCL = MCLs are expressed in concentration units (typically milligrams per liter [mg/L] or micrograms per liter [Âľg/L]) and are enforceable standards set by the U.S. Environmental Protection Agency (EPA) for various contaminants found in water. Cation resins that are shipped in the hydrogen form may be loaded with potable water or with soft water; however, it is better if they are loaded with previously deionized water. Anion resins shipped in the hydroxide form may be loaded with soft water, or better with deionized water. 58
Hydroxide-form anion resins should not be loaded with water that contains in excess of 5 parts per million (ppm) of hardness; otherwise, the final water quality realized when the resin is placed into service will contain traces of hardness. Applications where ultrapure water is required (such as nuclear power plants, microelectronics manufacturing, and pharmaceutical water) require scrupulous cleanliness and careful handling. Touching regenerated resin with a bare hand can add enough sodium and chloride (from sweat) to potentially prevent that resin from reaching its expected quality goals when placed into service. For these applications, it is best to wear protective outer garments such as Tyvek coveralls, hoods (or hair nets), and long-sleeved gloves. Minimize the time the resin is exposed to air, especially with mixed-bed and hydroxide-form anion resins, as these resins can be contaminated by carbon dioxide from the air. Any water used should be the same quality that the resin will be exposed to in use (in other words, ultrapure water for resins that will be used in ultrapure service). All devices, hoses, fittings, pumps, and scoops used should be pre-washed with ultrapure water before use. For everyday use, even in demineralizer applications, this level of concern is not needed, only for ultrapure water systems expected to make 18 megohms-cm or better resistivity and/or sub-parts per billion (ppb) levels of ionic impurities.
Documentation
When purchasing new resin, place a copy of the purchase order and the new resin analysis in a safe place where it will be accessible for many years. Take notes while loading resin (e.g., volume loaded [and lot numbers for larger tanks], date loaded) plus any notes regarding regeneration, issues, and things you would do differently next time. Resin replacements do not occur very often (typically three-year intervals or longer); people change jobs, and memories fade over time. Having a record of what and how things were done will be useful the next time to whoever oversees the next rebed. For any critical resin application, take a sample of the new resin (500 milliliter [mL] or more); label it with the product name, lot number, and date; and put it in a safe the Analyst Volume 27 Number 1
The next generation of scale inhibitor is here Aquatreat® AR-888 polymer, Nouryon’s patented technology, is a superior non-P calcium carbonate scale inhibitor in high LSI conditions with lower toxicity than existing alternatives. It utilizes all three polymer scale inhibition mechanisms – threshold inhibition, dispersion and crystal modification – to provide water treatment formulations with unmatched performance. Aquatreat AR-888 can be used in cooling towers as well as oilfield and mining production processes. Compared to competitive maleic homopolymers, its benefits include: • • • • • •
Extremely low toxicity Stronger calcium sulfate performance Better iron tolerance Easier formulation Equal bleach stability No need for additional dispersant in formulations due to its optimized molecular weight
To request a sample and learn more, contact us at ANSC-CS@nouryon.com or 800.906.9977.
Part 5: An Overview of IX Resins for Water Treatment continued
place. If there is ever a question about the resin, having retained samples will be helpful. Before throwing used resin away, if there is any doubt that it may have come in contact with something hazardous, have a sample analyzed (and save the analysis). Spent resins used in potable water and other purewater applications may not require analysis, but some landfills do. As far as sending resin to a landfill, make sure the resin is pH neutral and completely dewatered as many landfills will refuse to accept resin if water is dripping from the disposal containers, especially if that water has a particularly high or low pH.
Final Thought
This short discussion of IX resins provides closure to a multi-part work published this past year in the Analyst that covered storage, moving resins from place to place, loading, unloading, disposal, and step-by-step procedure outlines. The Appendix that follows this article provides an overview of procedures that should be followed in the use of IX resins. Peter Meyers is technical director for ResinTech Inc. Mr. Meyers is an IX enthusiast who was fortunate to fall into the field of IX in the early 1970s and has never attempted to climb out. His experiences include process design and detailed mechanical engineering of ion exchange systems, startups, troubleshooting, laboratory analysis, applications research, and technical support. He can be reached at pmeyers@resintech.com.
Appendix Procedures for Loading and Unloading Resin From Medium-to-Large Size Pressure Vessels Preface Procedures (related to loading and unloading IX resins) is an appendix to a five-part series of articles published in the Analyst that cover various aspects of how IX resins are used. Not the actual applications, but the physical aspects of touching resins, feeling them, and caring for them. Introduction Although detailed, step-by-step procedures have to be written on a case-by-case basis, the essential requirements remain the same for most processes related to IX resins. Detailed procedures aren’t always needed. For instance, when loading a small softener for residential use, the chance that a mistake will result in injury is pretty small, and about the worst that can happen is loss of time and money. Outlines help keep us focused on the correct path and can serve as a useful guideline, even for those of us who handle resins on a daily basis. For critical applications, step-by-step procedures become of paramount importance, especially those applications where a mistake could result in injury or worse. Here are outlines for the different steps in the use of loading and unloading IX resins.
Loading 1. Verify and record the following: a. Type of resin. b. Ionic form. c. Volume to be loaded. d. Tank that resin is to be loaded into. e. Water, power, drains, and workers are available. i. Water quality should be consistent with the type of resin being loaded. ii. Workers should be briefed on and understand their responsibilities. f. Crane, hoist, and forklift, if needed, are available. 2. Calculate desired resin height. a. Make a mark on the viewport or inside the tank or devise other method of verifying resin height.
This article is based on a paper presented by the author at the 2018 AWT Annual Conference, which was conducted September 26–29, 2018, in Orlando, Florida.
60
the Analyst Volume 27 Number 1
Part 5: An Overview of IX Resins for Water Treatment continued
3. 4.
Rinse all components thoroughly, including: a. Tank that will receive the resin. b. Loading bin. c. Loading pump and hoses. Assemble and test resin transfer apparatus: a. Fill bin with some water and pump into the tank. b. Check that the discharge hose or hook is tied off securely into the tank. c. Check that the water supply hose is securely tied off and pointing toward the bottom of the resin pump. d. Leave the bin with approximately 12 inches of water in it. e. In some cases, it is convenient to drain the tank back into the bin (thus saving water). To do this a return hose must be connected from the bottom of the tank into the bin. 5. Move resin containers into position. a. Wash off or otherwise clean the outside of every container to prevent contamination while loading. b. Open drums and pull liners back (or open supersacks and tie off one side of the liner). c. Take a 500-mL sample of each lot (stop if anything appears suspicious). 6. Pick up the first container and position over the loading bin. 7. Start the resin pump and water flow into the bin. a. Start dumping resin into the bin. i. Tip the drum or (slowly) open the bottom of the supersack. ii. If loading from smaller (1 cubic foot [ft 3] or 25 liter) bags, rest the bag on the edge of the bin and with a sharp knife, slice the bag up the belly, and dump it into the bin. Loading from small bags can be a bit messy and a pain. iii. It is important to control the resin flow and not add it too quickly. b. Keep the liquid level in the bin at or above the resin and always above the pump. i. Adjust water flow to maintain level. ii. If the pump needs to be stopped, pull it up out of the resin and allow it to pump only water until the hose clears. c. Keep the liquid level in the tank above the resin level but below the manway. 61
i. Drain water as needed to keep level from rising too high. d. Continue adding resin, one container at a time, until approximately 90% of the calculated volume has been added. i. Allow the water and resin to suck down to the bottom of the bin, then turn off the pump. e. Briefly backwash the resin in the tank (upward flow of water), then allow settling and check the level. f. Add additional resin if necessary to reach the desired bed height. 8. Continue adding water to the bin and pumping into the tank until all the resin has transferred into the tank. 9. Clean up the resin containers and any spilled resin. 10. Move on to any additional tanks that need to be loaded and repeat steps.
Unloading 1. Verify and record the following: a. Volume of resin to be removed. b. Which tank(s) the resin will be removed from. c. Sufficient containers are available to receive the resin. i. As a rule of thumb, double the resin volume is needed to allow for water inventory. ii. Containers must drain or have screened drains in them to allow for free water removal. iii. Spent resin fate. iv. For landfill disposal, the resin generally must be pH neutral and may require certification as nonhazardous. d. Water, power, drains, and workers are available. e. Workers should be briefed on and understand their responsibilities. f. Crane, hoist, and forklift are available. 2. The exact unloading procedure depends on the way the IX tanks are configured. a. For pressure vessels that have a resin outlet connection: i. Drain ALL the water from the vessel. ii. Remove the blind flange and attach a valve and hose (2 inches is ideal). iii. Place the IX tank into a slow backwash (upward flow of water). the Analyst Volume 27 Number 1
Part 5: An Overview of IX Resins for Water Treatment continued
iv. Open the resin outlet and allow resin and water to flow into the receiving container. v. Continue filling containers with resin until all the resin has been removed from the tank. b. For vessels that do not have a resin outlet but do have a top manway: i. Assemble a resin pump and discharge hose. ii. Attach a rope to the pump so that it can be lowered into the vessel. iii. Make sure there is plenty of hose to reach the receiving container. iv. Place the IX tank into a slow backwash (upward flow of water). v. Drop the pump down until it is partially submerged in the resin, turn it on and allow resin and water to flow into the receiving container. vi. Add water as necessary to keep the water level 6 to 12 inches above the resin level. vii. Continue dropping the pump and filling containers with resin until all the resin has been removed from the tank. c. For vessels that have neither a resin outlet nor a top manway, it is necessary to vacuum out the resin: i. Hire a vacuum truck to remove the resin or consult knowledgeable sources for advice. 3. Allow resin receiving containers to drip dry. a. Use a shop vac or other vacuum device to assist in dewatering. 4. Drain the IX tank completely, and verify it is safe to enter the confined space. a. A blower or other source of external air is advisable. b. Verify safety personnel are standing by and that workers have been trained on safety/rescue procedures. 5. Enter the tank and vacuum out the last traces of resin. a. This is an excellent time to inspect the underdrain for signs of wear or other problems. b. This is also an excellent time to inspect the lining. 6. Clean up any trash and resin spills. a. If new resin will be loaded in the near future, it is acceptable to leave the IX tank open and drained; otherwise, the manway and any open connections should be closed. 62
Definitions Resin pump
A submersible trash pump or eductor or double diaphragm pump. Double-diaphragm pumps are the least desirable because they are the most prone to plugging the transfer hose. Loading bin
Any plastic container comfortably larger than the containers of resin with an open top that the resin can be dumped into. In a pinch, the resin drums can be used as loading bins, but it is a bit tricky and can easily lead to loss of resin onto the floor. IX tank
The IX pressure vessel the resin will be loaded into. Hose
2-inch minimum pressure hose good for at least 50 psi and preferably smooth on the inside. Hook
A “U�-shaped piping assembly open on one end and connected to the hose on the other that can fit through the manway and into the tank securely. Water
Transfer water (30 to 50 gallons per minute [gpm]) is generally necessary, plus some means of controlling the flow and directing the flow toward the resin pump suction. Water used to load hydroxide-form anion resin MUST be softened or better. Supersack
A large bulk sack made of woven fiberglass intended to hold bulk solids. Most supersacks are larger than 25 ft3 and less than 45 ft3 in size and can weigh up to approximately 2,500 pounds when full of resin and/or water.
Water quality needed for loading (water quality needed for unloading is less critical, unless the resin will be reused): 1. Potable water can be used for salt-form resins (sodium-form cation resin and chloride-form anion resin). 2. Use soft water (<5 milligrams per liter [mg/L] hardness as calcium carbonate [CaCO3]) as a minimum for hydroxide-form anion resin (deionized [DI] water would be better). the Analyst Volume 27 Number 1
Part 5: An Overview of IX Resins for Water Treatment continued
3. Use DI water (<10 microsiemens per centimeter [µS/ cm]) for hydrogen-form cation resin and for hydroxide-form anion resin. 4. For resins used in ultrapure water service, use water of the same quality (or as close to it as possible).
Additional advice When loading from bags, rest the bag against the top edge of the bin, use a knife to slice open the belly of the bag, and then shake the bag to remove the resin. Use a fresh knife blade to cut cleanly and avoid strings or pieces of the bag from falling into the loading bin. When loading from drums, remove the lids ahead of time, remove the wire tie or other liner closure, and pull the liner down over the outside of the drum. Hold onto the wire ties and drum seals for proper disposal. If a forklift is available, use the lift to position a pallet of drums just about 12 inches off the floor. Then carefully tip the drum so it rests against the side of the loading bin. This will allow some of the resin to fall into the bin. Use buckets to finish emptying the drums into the bin, or tip the drum to remove the last bits of resin. If a fork lift is not available, use a bucket to transfer about half the resin from each drum to the bin, then pick up the drum and tip it over the side of the bin so that the resin falls into the bin. Do not attempt to lift full drums, as serious back injury could result. When loading from supersacks, if they have a bottom spout, this can be used to control the flow of resin into the bin. First, secure the straps of the supersack over the forks so that they cannot slide off. Use the forklift to pick up the sack and position it over the loading bin. Untie the bottom spout and either cut or untie the inner liner. Lower the forks so that the spout lowers into the bin, or use the drawstring to limit the flow of resin. If the sack does not have a bottom spout, position it over the bin, and then carefully cut the side of the sack to allow the resin to pour out. Gradually widen the hole to control the flow. When the sack is almost empty, use a hose to wash out the last bits of resin.
“When the sack is almost empty, use a hose to wash out the last bits of resin.”
What to do if the transfer hose plugs with resin? The slurry may become too thick and plug up the transfer line. When this happens, the clog can be cleared. 1. Unplug the resin pump. 2. Pull the pump up out of the resin. 3. Direct the water hose into the pump suction. 4. Plug the pump back in until the pumping action resumes. It may be necessary to repeat this (pump off, water on, pump on) several times. Each time, the resin should be allowed to flow back out of the line when the pump is turned off. You should notice increased pumping action with each cycle. This process feels something like “rocking” a stuck car out of the snow. If this does not clear the hose after several cycles, try the following approach: Remove the transfer hose from the pump and connect the hose directly to the pressurized water supply line of the appropriate quality, and open the valve to maximum. The full-line pressure will always unplug the hose. Flow may start slowly but will increase steadily until all the resin has been pushed out of the hose into the process tank. Once the line is clear, restart pumping the resin.
Closure These step-by-step procedure outlines are intended to accompany a much longer and more comprehensive work that describes in detail how resins are stored, loaded, unloaded, and disposed of. Please read Parts 1 through 5 before tackling this yourself, and, as always, consult knowledgeable sources for advice as necessary.
Ion exchange technologists never die, they just keep regenerating.
63
the Analyst Volume 27 Number 1
Technical Briefing
Can a Non-Chemical UV Dechlorination System Improve RO System Performance? R. Aaron Nickles, Southern Company—Plant Bowen
64
the Analyst Volume 27 Number 1
Georgia Power’s Plant Bowen, a 3,160-megawatt coalfired power station located in Cartersville, Georgia, has faced frequent reverse osmosis (RO) membrane and cartridge filter maintenance and replacement issues in recent years. The RO and cartridge filter system problems were caused by biological fouling and oxidation, despite the power station’s use of a sodium metabisulfite (SMBS) dechlorination process. As a result, on a trial basis, Plant Bowen tested three non-chemical, medium-pressure ultraviolet (UV) dechlorination treatment systemsA in March 2014, with the aim of improving the quality of the RO feedwater. Together, the three systems could treat a flowrate of 680 gallons per minute (gpm) (154 cubic meters per hour [m3/hr]) with a 95% UV transmittance (UVT), which is an indicator of water quality and represents the percentage of UV light passing through the water. These UV units were installed in series on existing stainless steel piping after the media filters and before the cartridge filters and RO trains. At the conclusion of the evaluation period two months later, UV dechlorination technology had effectively removed free and total chlorine from boiler feedwater to undetectable levels (below 0.02 ppm) from inlet free and total chlorine levels above 1 part per million (1). Free available chlorine (FAC) levels at or below 0.1 ppm are required to protect the RO membrane elements and ensure optimal performance. Following the successful test, the decision was made to incorporate this technology into the plant’s water treatment system. As a non-chemical approach to decomposing the free chlorine oxidant and protecting the RO membranes, this UV dechlorination method allowed the facility to reduce or eliminate the use of SMBS and reduce maintenance and associated costs. Data for the membrane system’s differential pressure (DP), normalized salt passage and rejection, permeate flow, and normalized permeate flow under the use of the technology was analyzed for a 940-day period from August 2014 to February 2017.
Plant Process and Operations
Plant Bowen receives its source water from the Etowah River. Following clarification and multimedia filtration, water passes through a two-stage cartridge filter process before becoming feed to the RO system. The two-stage micron (µm) filter treatment step is composed 65
of two trains, each containing a 3-µm filter followed by a 1-µm filter. The RO system consists of two 250-gpm (114 m3/h) trains (Train A, Train B) containing 72 membranes per train. The RO system is arranged in a double-pass configuration with 48 membranes in the first pass, followed by 24 membranes in the second pass. The facility samples twice a week for feedwater quality (pH and turbidity) and permeate and concentrate values of the RO system. Given the plant’s problem with microbial growth and the creation of a biological matrix in the RO filters that restrict flow, differential feed pressure, effluent pressure, normalized flow, and chlorine residual are measured daily. A 10% increase in differential pressure alerts operational staff to undertake a cleaning of the membrane system with a caustic and acid solution. The membrane-cleaning process requires the facility to run at half capacity for 48 hours since each train is taken offline for a 24-hour period to have the membranes rinsed before being returned to service.
UV Technology Operational Principles
The medium-pressure UV technology is a physical process for disinfection that exposes bacteria, viruses, and protozoa to germicidal wavelengths of UV light, measured in nanometers (nm), to render them incapable of reproducing or further infecting a water system. Through UV oxidation, UV light can also destroy chemical contaminants. The technology measures four critical parameters, including UVT%, flowrate, UV lamp intensity (kilowatts [kW]) and apparatus (consisting of total internal reflection [TIR] and dose facing) in real time to maintain a specified UV dose. The system uses a TIR-based apparatus that, when coupled with the comprehensive monitoring of critical parameters, allows the system to achieve and maintain the specified UV dose. The system’s TIR technology, which is similar to fiber optic science, recycles UV light energy within the chamber. Simply put, the UV wavelength is effectively lengthened (i.e., magnified) and provides a greater opportunity to inactivate microorganisms. The core of the technology is its water disinfection chamber made of high-quality quartz surrounded by an air block instead of traditional stainless steel. This configuration uses fiber optic principles to trap the UV light photons and the Analyst Volume 27 Number 1
Can a Non-Chemical UV Dechlorination System Improve RO System Performance? continued
recycle their light energy. The photons repeatedly bounce through the quartz surface back into the chamber, effectively lengthening their paths and their opportunities to inactivate microbes.
Long-Term Membrane Performance
Plant Bowen uses a five-year replacement cycle for the RO elements; the last full installation occurred in March 2014. The HOD UV system was also installed and placed into continuous operation in March 2014. After three years of operation, the RO membranes were operating at the same level as new elements. In 2019, it was necessary to replace the RO membranes due to an over pressurization from a potential operator's error. Data for the membrane system’s differential pressure, normalized salt passage and rejection, permeate flow, and normalized permeate flow under the use of the chemical-free UV dechlorination system was analyzed for a 940-day period from August 2014 to February 2017 (Figures 1 to 4). Normalized permeate flow is higher compared with a new membrane, while the quality of the permeate (salt passage and rejection) is similar to a new membrane. Figure 1: Train A DP during 940 days of operation.
66
the Analyst Volume 27 Number 1
Can a Non-Chemical UV Dechlorination System Improve RO System Performance? continued
Figure 2: Train A normalized salt passage and rejection during 940 days of operation.
Figure 3: Train A normalized permeate flow during 940 days of operation.
67
the Analyst Volume 27 Number 1
Can a Non-Chemical UV Dechlorination System Improve RO System Performance? continued
Figure 4: Train A permeate flow, feed pressure, and feed temperature during 940 days of operation.
Prior to the installation of the dechlorination UV system, the membranes were cleaned one to two times per month; following the installation of the technology, the clean-in-place (CIP) frequency was reduced to once every two months. What’s most interesting is that the driver for cleaning the membranes has also changed. After three years of operation, the membranes were only up to 34 pounds per square inch (psi) differential pressure from the original 27 psi when they were put into service. This change indicated a longevity of the membrane elements that didn’t exist without the use of the UV dechlorination technology. Comparatively, the pre-2014 membrane elements were running at a 50 psi differential pressure after three years of operation. Performance of the cartridge filtration system has also been enhanced with the use of the dechlorinating UV technology, and there has been a reduction in cleaning frequency that has resulted in an annual cost savings of $60,000 to $80,000. Prior to the installation of the system, replacement costs averaged $100,000 to $120,000 per year. This is shown in Table A.
68
Table A: Cartridge Filter Replacement Frequency and Annual Cost
Year
3 µm Total Replacements
1 µm Total Replacements
Total Replacement Cost*
2015
10
0
$100K
2016
2
2
$40K
2017
2
2
$40K
*The cartridge filter system consists of 3-µm and 1-µm filters. There are two vessels of the 1-µm filters and two vessels of the 3-µm filters. Each vessel holds 52 filter elements, so there are 104 3-µm filters, and 104 1-µm filters, which are always changed in pairs (Train A, Train B). The replacement cost for a vessel of 52 filters of either cartridge type is approximately $10,000. Since the installation of the non-chemical UV dechlorination technology, the chemical feedrate has decreased by 75%. Before the change in 2014, the power plant was originally feeding SMSB at 4 parts per million. The 2017 feedrate was 1 ppm. The monthly chemical usage has been reduced from 44.2 gallons per month in 2013 to 7.6 gallons per month in 2017. The facility has realized an annual cost savings of $5,000 with the reduction in chemical usage. the Analyst Volume 27 Number 1
Can a Non-Chemical UV Dechlorination System Improve RO System Performance? continued
Conclusion
Incorporating the non-chemical water treatment technology into full-scale operations at Plant Bowen has aided dechlorination efforts at the facility. In addition to reducing the use of SMBS, the facility has also minimized the frequency of microfilter replacement and CIPs for RO membranes. Moreover, there has been no reduction in performance of the RO membranes with the use of the UV dechlorination technology. As a result, Plant Bowen has been able to maintain the integrity of feedwater for the boiler and steam cycle, ensuring production and quality levels necessary for the power plant to operate efficiently.
Reference
1. EPRI (2014). “Boiler Makeup Water Dechlorination Using Advanced UV Technology at Plant Bowen Water Research Center, Report # 3002002146, Electric Power Research Institute, Palo Alto, CA.
Endnote
The UV technology referred to in the text is known as Hydro-Optic™ (HOD) UV. It is offered by Atlantium Technologies Inc. In the text, it is referred to as the non-chemical UV water treatment technology.
A
Aaron Nickles is a senior maintenance specialist at Georgia Power’s Plant Bowen in Cartersville, Georgia. He joined the company in 1988 and served as a senior chemistry tech until 2016, when he moved into his current position. Mr. Nickles holds a B.S. in biology from Shorter University (Rome, Georgia). This paper was presented at the Electric Utilities Chemistry Workshop, which was conducted June 5–7, 2018, at the University of Illinois in Champaign, Illinois.
70
the Analyst Volume 27 Number 1
SUPPLIER OF THE YEAR
Bringing Quality Blending To The West Coast QualiChem is proud to announce the opening of our new
No Direct Sales
precision blending facility in Verdi, Nevada. We are now
Precision Manufacturing
better positioned to provide our customers with industryrecognized benefits and services coast to coast. Just one more way we are demonstrating how‌
The Blender Matters 800.296.9102 | www.qualichem.com AN ISO 9001:2015 COMPANY
Formulatory Expertise Application Support Custom GHS-Compliant Labels and SDSs
Membership Benefits
Demystifying Cooling Water Online Monitoring and Control Platforms
AWT Bookstore
AWT’s Cooling Water Subcommittee recently developed a paper in response to an expressed need for clarification of online monitoring and control platforms. The speed at which technology is overtaking our lives is growing exponentially each year. Technology has even made its way into the relatively stable and unchanging universe of Cooling Water Treatment. The increased use of technology in the water treatment industry is being driven by a need to respond to several important trends. These include increased regulations, a need for greater access to information, and tightening resources. You can read the complete paper on the Members Only portion of the AWT website at www.awt.org.
Attention members! Don’t forget that the AWT bookstore is the preferred information resource for industrial and commercial water treatment professionals. The bookstore offers several items for immediate purchase, including the Technical Reference and Training Manual, a variety of textbooks, and the AWT slide rulers. Visit the bookstore online at www.awtstore.org for a complete listing of available publications, item descriptions, and order forms.
Get Involved!
AWT has a welcoming and dedicated group of volunteers who help develop materials, programs, and services for members, and we are always looking for new people to get involved. Our committees work on various projects in the pipeline. Participating on a committee introduces you to water treatment professionals and suppliers nationwide, better establishing you in the industry. We need your skills, excitement, and diverse perspectives to lead our community. To work on a project or join a committee, contact us at (240) 404-6477 or visit our website at www.awt.org.
72
the Analyst Volume 27 Number 1
Association News
Charity Update
Following is the Activity Advancement Report for AWT-Sponsored Communities in Las Uvillas, La Union, and El Horconcito, Hondouras
October 2019 Pure Water for the World (PWW) board members and PWW Honduras project coordinators visited the mayor of Maraita and his team to officially communicate the commencement of PWW’s work in Maraita, including water, sanitation, and hygiene education. The group discussed the initial project with the three AWT-sponsored communities: Las Uvillas, La Union, and El Horconcito. November 2019 Baseline data was collected in each of the communities and is being reviewed to check that there is no missing information. After reviewing the surveys, PWW will analyze the data to set standards for measuring the impact that the project has on these three communities. Community leaders were identified and invited to a meeting to discuss the project goals and project steps and to build their understanding and confidence about the project. This contributes to the overall success of the project. During this initial meeting, community leaders received their first assignment, which was to distribute invitations to each family for the forthcoming meeting, during which PWW will present the project to the all community members.
December 2019 Materials were purchased for trainings and for filter installation. Socialization was done in all three communities with all families. Home hygiene trainings and Community Agent trainings were conducted for families in all three communities.
73
the Analyst Volume 27 Number 1
Industry Notes New Staff at ProChemTech International ProChemTech International, Inc. is pleased to announce that Mark Smedley has been appointed to the position of district manager for our Pittsburgh District. Mark will be responsible for district sales and service covering southwestern Pennsylvania, southeastern Ohio, and northwestern West Virginia, working from his home office in Cranberry Township, Pennsylvania. Mark is a veteran water treatment technologist, having worked for Prominent Pump in customer service for many years.
ProChemTech is pleased to announce that Thad Schuster has been promoted from Pittsburgh district manager to corporate sales and service manager, Brockway, Pennsylvania. Thad is replacing Vickie Jacklin, who has retired after 28 years of service with the company. Thad will work with sales and marketing employees on a national basis and develop additional accounts in the Brockway area, and will be responsible for maintaining our traditional high level of customer field service. Thad has been the Pittsburgh district manager since 2015 and previously completed six years in the U.S. Marine Corps. ProChemTech provides innovative, integrated water management programs for boiler, cooling tower, process, and wastewater systems to commercial, government, and industrial customers in 14 states. Chemical product applications are supported by onsite service, while the majority of the cooling tower, industrial wastewater treatment, and reuse and recycle systems are supplied as custom design-build projects. Chemical products and equipment are manufactured in our Apache Junction, Arizona, and Brockway, Pennsylvania, plants. Additional information can be found at www.prochemtech.com
LANXESS Makes Dimensioning Tool for Water Treatment Even More Practical
The specialty chemicals company LANXESS has comprehensively updated its LewaPlus design software for the water industry. The dimensioning of reverse osmosis (RO) and ion exchange systems (IX) is now even more practical and user-friendly. There is also the option 74
H2O to include ultrafiltration (UF) in the planning. The new UF module was presented for the first time at Aquatech, in November 2019 in Amsterdam.
H SO
Ultrafiltration is used as pretreatment for RO—and 2 4 increasingly for IX resin applications. Around one-third of all newly built RO systems have upstream ultrafiltration—and the number is rising. LANXESS is a global distributor of high-quality Gigamem UF membranes and systems from French company Polymem, which is based in Toulouse. To design complex water treatment systems that also include ultrafiltration technology, LANXESS has now integrated this pretreatment into its software. UF purifies and disinfects water in a single step. It is an alternative to conventional filtration in water purification and produces filtrate with a water quality that is considerably more consistent. UF often also replaces other conventional treatment techniques as well as microfiltration, as it also removes smaller particles and thus significantly reduces deposits in subsequent process steps. This enables a more stable process. LewaPlus also offers users the option to create their own water library. This is because customers often have only an incomplete water analysis—if they have one at all— when planning their system. With a library, they can then utilize the data that is stored in LewaPlus. “We are planning to expand on the master data to include additional water types. There are even already parameters in place for the quality of seawater from various regions,” explains Dr. Jens Lipnizki, head of Technical Marketing Membranes in the Liquid Purification Technologies (LPT) business unit. LewaPlus is already being used in 90 countries on six continents, including by Centec, a leading systems provider of technologies for water treatment and the Analyst Volume 27 Number 1
Industry Notes continued
degasification that is based in Maintal near Frankfurt am Main. User Bernd Hackmann says that “for many years now, I have been using LewaPlus regularly to design complex water treatment systems for a wide variety of sectors. The option to combine various technologies in the system design is a real advantage. I am already looking forward to the new module because the announced direct cost comparison of the various designs will provide an additional benefit.” The new calculation options are available in LewaPlus for all ion exchange resins modules, thus enabling a cost comparison of various system designs and processes. These expand on the existing cost calculation for RO systems. Using identical calculation parameters makes it possible to carry out a direct comparison of the costs of RO and IX systems. “To our knowledge, this function is unique,” says Lipnizki. Detailed information on products and services can be found at http://lpt.lanxess.com.
Kemira Wins Award for Utilizing Recycled Byproducts as a Raw Material in Drinking Water and Wastewater Treatment Products
Kemira has won the European chemical industry’s prestigious Responsible Care award for environmental responsibility. It was awarded by CEFIC (The European Chemical Industry Council) to Kemira´s ferric sulphate plant in Pori (Finland), which utilizes recycled industrial byproduct in its drinking water and wastewater treatment products. Through this project, Kemira’s expertise in chemistry is helping to create the foundations for a circular economy. Before 2017, Kemira’s plant in Pori received ferrous sulphate as the main raw material from a titanium dioxide plant in the same industrial area, where ferrous sulphate is formed as a byproduct. In January 2017, ferrous sulphate supply from the plant was interrupted, and to ensure the continuous availability of raw material, Kemira investigated the ferrous sulphate landfill nearby that had accumulated from excess unused side-streams from titanium dioxide production. Already in 2017, Kemira was able to utilize 27,000 tons of ferrous sulphate, while the estimate for the production volume in 2019 is as high as 170,000 tons. Following a
successful testing period, Kemira is now utilizing a landfill that contains several million tons of ferrous sulphate raw material, putting some 30 years of accumulated industrial byproduct back into use, and securing supplies for many years to come. “While the water treatment industry is adept at using industrial side-streams as raw materials for sourcing metal compounds, this project shows that there is much more potential available. As the best byproduct streams have been harnessed—for example, scrap iron and spent pickle liquor—many other valuable streams are literally going to waste,” says Rasmus Valanko, director of corporate responsibility. Already today, 70–80% of all raw materials used in Kemira’s coagulant products used for water treatment are recycled byproducts from other industries. The amount of water treated with Kemira’s products is equivalent to the annual water consumption of 320 million people. For more information, visit www.kemira.com.
MFG Chemical Adds to Logistics Team; Launches Software Program; Celebrates Customers
MFG Chemical, a provider of specialty and custom chemical manufacturing, added to its domestic and international customer service and logistics staff. Having hired international and customer service professional Kim Curtis earlier this year, MFG Chemical has now added logistics expert April Goins to the domestic service team. Goins brings experience in negotiating freight rates and tracking shipments, saving customers’ time and money. Prior to joining MFG Chemical, Goins developed her skills as a logistics coordinator and team manager at Universal Marketing Systems and Beaulieu Commercial. She earned numerous certifications in customer service and leadership. The company implemented its operational excellence software program, OESuite. OESuite improves information and workflow management, resulting in better organizational alignment, production operations, risk assessment and mitigation, maintenance, and employee safety. continued on page 76
75
the Analyst Volume 27 Number 1
Industry Notes continued
AquaPhoenix Hires Additional Team Members to H2trOnics
AquaPhoenix is excited to announce several strategic new hires in the H2trOnics Equipment Division. Most recently, Tom Tinney has come on board as a Technical Sales and Product Support Specialist. Tom is part of the growing support team and brings over 20 years’ experience to AquaPhoenix with direct, hands-on experience in the water treatment industry. Tom is actively involved in the AWT Training Program and is currently the Fundamentals and Application Feed and Control Equipment instructor.
MFG Chemical also celebrated International Customer Service Week under the theme “The Magic of Service.” “It’s wonderful that MFG takes the time to show appreciation to its frontline service members who are providing world class service and to show appreciation to our customers for their support in 2019 and loyalty going into 2020,” said Customer Care Manager Kim Curtis. “We appreciate our customers and strive every day to add value to our customers’ end-use products by providing the highest quality, performance-enhancing chemistries and deliver them in the safest and most cost-efficient way through a dedicated and highly professional customer service and logistics team,” said Keith Arnold, president and CEO of MFG Chemical and member of the SOCMA board of governors.
Jake Smith joined the team in 2019 as Sales Account Manager. Jake has years of experience within the water treatment industry and his technical knowledge of chemical feed and control equipment will allow H2trOnics to continue to provide excellent service and guidance to customers. Jake is also a member of the AWT serving on the Young Professionals Committee and teaching various webinars. Sheldon Adcock also joins as the General Manager where he will work closely with customer service and technical support teams. Sheldon brings nearly 28 years’ experience in the oil, gas, and complex-specialty manufacturing environment. Sheldon’s experience will blend well with H2trOnics’ unique fabrication and product niche in the water treatment industry. These new members of the AquaPhoenix family will join in driving the culture of continuous improvement and growth. Please look for them to be actively involved with many AWT functions and leadership.
76
the Analyst Volume 27 Number 1
CWT Spotlight
Tyler Cooper
Water Treatment Consultant. Premier Water & Energy Technology, Inc. Jacksonville, Florida
What prompted you to obtain your CWT and when did you begin the process by taking the test? My familiarity with AWT and the certification came soon after I started working in the field for Premier. A few of my colleagues were CWTs, and we were all encouraged to consider including becoming a CWT as one of our goals. I began reviewing the requirements and studying for the test one year before I was eligible to become a CWT and scheduled the exam. My employer was supportive and provided educational material. Taking the test was the hardest part of the process. Experiencing the technical training prior to the test was beneficial as well and allowed an opportunity to discuss the test with my peer group. What advice would you give those thinking about taking the exam? My advice to those considering taking the exam is to view it as a means to advancing your career, and take advantage of the opportunity to differentiate yourself from the majority of your competition. Don’t wait to schedule the test until you feel completely comfortable. Whether you pass or fail, you will gain knowledge that will benefit you moving forward in your career. Make studying for the test a priority and commit to a date. There are a lot of great resources provided by AWT, including online programs/quizzes and the technical trainings that are applicable. Review the study habits with colleagues and peers who have already taken the test.
Why do you feel this credential was important to have? I was motivated to become a CWT by a few factors. I started in the water treatment industry soon after graduation, and as a result had minimal experience compared to colleagues and competitors in my region. Nothing can replace the knowledge gained through experience in our industry, but studying for the test accelerated the exposure to many different topics within the water treatment industry that I would not have encountered as quickly if becoming a CWT were not a priority. The majority, if not all of our customers, prospects, and trade associations are aware of the credential, and it increases the value you provide to your team. How has your CWT improved your professional career? The importance of becoming a CWT rises steadily as awareness of the certification continues to increase. Thanks to the efforts by member companies and suppliers within AWT as well as the association itself, it is not uncommon to see a CWT in addition to or as an alternative to a science degree as a prerequisite in bid specifications. Becoming a CWT has removed some barriers to entry and expanded the qualifications and strength of our resources available behind our team when pursuing new business. It also sets the stage for continuous improvement to maintain the certification, which is critical in our industry, as the bar is constantly being raised.
Congratulations to Our Newest CWT Please join us in congratulating the latest individual to become a CWT (November 6, 2019–January 31, 2020) Danial Farnham, CWT, Gurney Water Treatment NE
77
the Analyst Volume 27 Number 1
Making a Splash
Matt Haikalis, CWT Technical Sales Director APTech Group, Inc. West Chester, Ohio
What prompted you to start volunteering with AWT? Starting my career in early 2001 with a company that was active in AWT, I began to immediately see the impact that AWT has had in the industry. From technical papers to calculation tools, selection charts to the annual convention, these resources have helped me become informed to make good decisions and analyses for situations that arose within the customer base we were serving. The impact of that created a sense of giving whatever I can provide to help the next generation of water treatment professionals and organizations to be successful in providing value-generating, consultative advice and technologically and economically feasible solutions to the end users. The opportunity to volunteer has given me the chance to extend beyond just contributing to my own organization’s success (here at AP Tech) along with our valued customers to the industry as a whole. On a personal level, it allows my passion for water treatment to be fully maximized by being able to work alongside the industry leaders.
78
Why would you encourage others to become a volunteer? We all have something to contribute to the greater good of the industry. There are so many talented professionals in the industry that can make a difference, and volunteering provides an opportunity to really benefit to the industry as a whole. As we continue transitioning to a focus on water safety, water conservation, and water reuse/recycling, AWT needs to continue pulling from the knowledge and experience base of its members. Volunteers make it happen! How have you been able to utilize the expanded business connections you’ve made while volunteering? Certainly, the networking opportunity within AWT is invaluable, and volunteering provides access to a wide variety of people and organizations, which opens doors. Having now worked in two different facets of water treatment—from providing solutions to end users to now providing technology and value to water treatment solutions providers—volunteering has provided insight into the capabilities of the organization’s members and creates a greater chance to collaborate and identify potential opportunities.
the Analyst Volume 27 Number 1
Capital Eyes
EPA Revises Rules for Storing Chemicals The Environmental Protection Agency (EPA) has weakened an Obama-era rule governing how firms store some chemicals. Under the new standards, companies will not have to provide public access to information about what kinds of chemicals are stored on their sites. They also will not have to undertake several measures aimed at preventing accidents, such as analyzing safer technology and procedures, conducting a “root-cause analysis” after a major chemical release, or obtaining a third-party audit when an accident has occurred.
Background
On November 20, 2019, the EPA administrator signed the Risk Management Program (RMP) Reconsideration final rule, which modifies the existing rule to remove what EPA cited as “burdensome, costly, unnecessary amendments while maintaining appropriate protections and ensuring first responders have access to all of the necessary safety information.” The rule also resolves important security concerns. EPA Administrator Andrew Wheeler said the revised “Risk Management Program” rule addresses concerns raised by security experts, who feared that releasing the location of the country’s chemical stores could provide a roadmap for terrorists, as well as others. The changes are intended to promote better emergency planning and public information about accidents and maintain the trend to fewer significant accidents involving chemicals regulated under the RMP rule. The changes reflect issues raised in three petitions for reconsideration of the RMP amendments and addresses other issues that EPA believed warranted reconsideration.
Details
Specifically, the final rule addresses the following: Potential security risks associated with new information disclosure requirements introduced in the final amendments rule. 79
The Bureau of Alcohol, Tobacco, Firearms and Explosives’ (ATF’s) finding that a key incident affecting U.S. chemical safety policy (a fire and explosion in west Texas) was caused by a criminal act (arson) rather than the result of an accident. Concerns with the costs of the amendments rule. Concerns that EPA did not adequately coordinate its rulemaking with OSHA. EPA therefore made changes to the RMP amendments final rule to: Maintain consistency of RMP accident prevention requirements with the OSHA Process Safety Management (PSM) standard. Address security concerns. Reduce unnecessary regulations and regulatory costs. Revise some compliance dates to provide necessary time for program changes.
Specific Changes
Some of the changes in the final rule include the following: Rescinds all major accident prevention program provisions of the RMP amendments rule (e.g., thirdparty audits, safer technology and alternative analyses, incident investigation root cause analysis), and most other minor changes to the prevention program. Rescinds the public information availability provision of the RMP amendments rule.
the Analyst Volume 27 Number 1
Capital Eyes continued
ƒ Retains the requirement to hold a public meeting within 90 days after an accident, but only applies the requirement to accidents with offsite impacts. ƒ Modifies the exercise provisions to give more flexibility to regulated facilities and local emergency responders in complying with these provisions. The rule also rescinds the requirements for an owner or operator to provide, within 45 days of receiving a request by any member of the public, specified chemical hazard information for all regulated processes. This was rescinded because the consolidation of the required chemical hazard and facility information could highlight the vulnerabilities of a facility and potentially increase the risk of a terrorist attack on some facilities.
Future Accident Prevention
Accident prevention is a top priority at EPA. This final rule retains all of the prevention provisions that have resulted in the long-term trend of fewer significant chemical accidents, which have declined more than 50%
80
since the original requirements were put in place in 1999. The data demonstrates that the original RMP rule is effective at detecting, preventing, and mitigating accidental releases. From 2007–2016, at least 90% of RMP facilities had no reported accidents and nearly half of accidents occurred at less than 2% of facilities reporting multiple releases. EPA is prioritizing inspections and enforcement on high-risk facilities and in 2018 entered into the largest-ever settlement in the history of enforcing the RMP rule, valued at approximately $150 million. For more information on the final rule, visit https:// www.epa.gov/rmp/final-risk-management-program-rmp-reconsideration-rule. Janet Kopenhaver is president of Eye on Washington, and serves as the AWT Washington representative. She can be reached at (703) 528.6674 or janetk@eyeonwashington.com.
the Analyst Volume 27 Number 1
Financial Matters
Asset Protection Is Just as Important as Tax Planning Like many financially savvy individuals, you’re probably already thinking about filing your tax return. But don’t overlook another critical and equally important aspect of financial planning: asset protection. Here are some fundamental strategies to consider.
Buy Liability Insurance
Liability insurance policies help protect your assets from the financial risks associated with personal liability that results from an adverse legal judgment. Auto and homeowner’s policies, for example, usually include some liability coverage. Increasing your liability coverage beyond the standard amounts will provide additional asset protection. Personal liability umbrella insurance can give you even more liability coverage above the limits of your auto and homeowner’s policies. For instance, if you were sued for causing a car accident or found liable for injuries suffered by a visitor to your home, umbrella insurance could provide coverage up to the policy limits (such as $1 million).
Look to Statutory Protection
Federal or state law exempts certain kinds of property and assets from creditor liens. Thus, some assets you own may automatically be protected due to statutory guidelines. Qualified retirement plans are this type of asset, as are IRAs and 401(k) plans, life insurance proceeds, and Section 529 college savings plans. But keep in mind that inherited assets may not have the same degree of protection. The amount of home equity that’s protected (generally called the “homestead exemption”) depends on state law. In some states, it’s very generous, but in others, it’s extremely limited, given the value of homes today. In a couple of states, there’s no protection. Consult with an attorney about your state’s laws.
Establish a Trust
effectively relinquished control over the assets and put them out of reach of your creditors. The asset transfer must be done in advance of the act that created the liability, or the transfer could be nullified. In other words, the time to think about setting up such a trust is before you need to take advantage of it. An irrevocable trust also can help you protect assets for your children and grandchildren. Consider structuring the trust in a way that effectively gives future generations the benefit of the assets without transferring ownership of them to your heirs. This can shield those assets from your descendants’ future creditors. If you decide to use trusts as part of your asset protection strategy, remember that they may be subject to higher income tax rates and additional tax filing requirements. Trusts also may be costly to set up and require expert legal counsel to administer and maintain.
Obtain Expert Assistance
The details involved in implementing asset protection strategies can be complex. We can offer you guidance in your case. © 2019 Thomson Reuters
Asset Ownership Structure Is Key Ownership of your assets plays an important role
in whether they can be seized by creditors. Thus, it
might be wise in some situations to transfer ownership of certain assets to your spouse. If you’re at a
high risk of liability—for example, you’re a business owner—one strategy might be to retain ownership
of assets with statutory protection, as mentioned in
the main article, and transfer ownership of all other
Assets placed in an irrevocable trust can’t be removed, nor can the trust terms be changed. Thus, you’ve
assets to your spouse.
82
the Analyst Volume 27 Number 1
Business Notes
Cybersecurity for Small and Mid-Sized Businesses By Benjamin Orsatti, Esq., Associate General Counsel & Senior HR Consultant, East Coast Risk Management “Cybersecurity” is a bit like plumbing: most everybody thinks it’s a great idea, but we don’t really give it much thought beyond that until something goes horribly wrong, like a data breach. It’s easy to be lulled into a false sense of security, especially if you’re not a corporate giant like Yahoo, Equifax, Target, or Uber. “Why would a hacker want to steal data from little-old-me?” Oh, really? So, you’ve never been tempted to peek into your friend’s medicine cabinet while using their bathroom? In fact, a 2015 study determined that 43% of intentional data breaches (“cyberattacks”) have had small businesses as their targets. (Evan Kline, How to Navigate Cybersecurity in 2018 Directions to Guide Your Efforts, Pa. Law., March/ April 2018, at 30). And it wouldn’t be surprising to find that proportion to have increased since then, as larger companies have been retaining sophisticated technology firms to protect their customers’ and employees’ data. What to do, as a small or mid-sized company, depends first on where your business operates. If you do business in a jurisdiction that has its own data protection laws, you might not have a choice as to whether or not you’re going to implement a cybersecurity program—you have to! The European General Data Protection Regulation (GDPR) can be frightening—penalties for noncompliance can reach up to 4% of a company’s global revenue, or $22.5 million dollars (whichever is greater). This is why you want to cap your GPDR liability. If you anticipate doing a substantial amount of business in Europe, you may want to consider “self-certifying” under the EU-U.S. and Swiss-U.S. Privacy Shield Frameworks. Because this process involves an audit from the certifying agency, you’ll definitely want to secure both legal and technical help in advance to prepare for this audit. The International Association of Privacy Professionals (IAPP), for example, was one of the first organizations to offer both training and certification. Other training resources and certifications are also available, depending on a business’s specific needs.
83
Once completed, however, certified organizations are presumed to have “adequate” privacy protections for purposes of the GDPR, and EU Member State requirements for prior approval of data transfers are either waived or approval will be automatically granted. If you don’t expect to be in possession of protected European data on any more than an occasional basis, you’ll still want to be prepared when your European client or customer presents you with a GDPR-compliant Data Protection Agreement (DPA) to sign. In that case, you’ll at least want to have the following “minimum” protections in place: Pseudonymization, which refers to a data management and de-identification procedure; Encryption; Ensuring the ongoing confidentiality, integrity, availability, and resilience of systems and services processing personal data; Ability to restore the availability and access to data in a timely manner in the event of a physical or technical incident; and Processes for regularly testing, assessing, and evaluating the effectiveness of technical and organizational measures for ensuring the security of the processing. 26.04[14], Compliance Checklist for U.S. Businesses, 3 E-Commerce and Internet Law (2019 update). So far, so good. But this is America. We don’t bother with all that, right? New York and California have already passed their own data protection laws, so it may only be a matter of time before the trend spreads inland (I’m looking at you, Kansas!).
the Analyst Volume 27 Number 1
Business Notes continued
California (state motto: “Keeping lawyers gainfully employed since 1850”) passed what may be the most stringent data privacy law in the country in June 2018 (effective January 1, 2020)—the California Consumer Privacy Act, Cal. Civ. Code § 1798.185(a). This law is crafted in terms of “rights.” Specifically, consumers will have the “right” to: Request that a business disclose the categories and specific items of personal information that it collects about them, the sources of information collected, the business purpose for said collection, and categories of third parties with whom the information is shared; Request that a business delete any personal information related to the customer; Demand that a business not discriminate against them if they choose to demand that the business not pass along their information to third parties; and Notification of their rights through issuance of privacy policies. To prepare for potential data breaches, there are steps that a small-to-mid-sized business can take without having to create an IT department from scratch. The most fundamental of these steps is what is known as “data mapping.” You’ll want to document where data flows throughout an organization from the moment it is collected to where it is stored to the third parties with whom it is ultimately shared. In doing this, you’ll be creating an “inventory” of what data is held where. If a customer or employee demands that data be provided or destroyed, or both, you’ll then be able to find it and ensure that it stays put! If you’re keeping your data security “in-house,” the employee or employees appointed to this task should be able to, at minimum, ensure that: Your server is patched with the latest security updates; Your network is running an advanced firewall;
Regular backups are made; and The appointed employees receive regular security training. Finally, you may be operating a business where your employees are given technology to take home with them. Fraught with peril, this is! Employees should be trained, at work and at home, on basic principles of “password hygiene”—nobody should be taking home a laptop, the password to which is “[employee or employer name]123.” If you’ve not opted for “two-factor authentication,” any device used by any employee that might contain company, customer, or employee information should be accessible only by means of a “strong” password and must have the capability to be “wiped” of all data remotely immediately upon discovery that the device has been lost or stolen. In short, everybody in your organization—from the CEO to the temporary seasonal help—should be trained on the best practices for protecting sensitive information. The practices should be documented in policies that are distributed and explained to all. Deviation from these policies should be subject to discipline in just the same manner as any other policy violation, as the risk of harm to the company is just as great. That’s not so hard, is it? If you are an employer with questions about this or any issue relating to safety, human resources or workers’ compensation, contact East Coast Risk Management by calling (724) 864-8745 or emailing us at hrhelpline@eastcoastrm.com. Disclaimer: The information provided on this website is for informational purposes only and not for the purpose of providing legal advice. Use of and access to this website do not create an attorney-client relationship between East Coast Risk Management or our employment law attorney and the user or browser. The post Cybersecurity for Small and Mid-Sized Businesses appeared first on East Coast Risk Management.
Someone is reviewing server logs to detect suspicious behavior;
84
the Analyst Volume 27 Number 1
T.U.T.O.R.
Technical Updates, Tips, or Reviews
How Often Should I Test My Water? By Tim Daniels, Chem-Aqua Inc.
Water treatment professionals are frequently asked, “How often do I need to test the water in my system?” There is no standard answer to this question since it is as varied as the water qualities that different systems treat. A number of factors need to be considered when determining what is “reasonable and customary” for each facility. In a typical facility, some of these general factors are illustrated by the following seven questions: 1. What type of system is being operated? 2. How critical is the water treatment system to the operation of the facility? 3. Where is the facility located? 4. What are the realities of staffing availability and training?
A number of different methods of testing are also used throughout the industry, including drop titration (Figure 1), digital titration, colorimeters (Figure 2), handheld meters, and color comparators. Generally, the parameters being tested and the method the water treater is most familiar with determines what method is used. For example, when testing metals, colorimeters are necessary; but for pH, both color comparison methods and colorimeters can be used. Each method has strengths and weaknesses. Some methods, such as tests using colorimeters, are more accurate but take more time to complete, while other methods, such as drop titration, are much quicker to perform but have a larger margin for error.
Figure 1: Example of a drop titration testing kit.
5. Is testing frequency mandated by any regulations, outside consultant guidelines, or company policy? 6. Does the facility have a Water Management Plan (WMP)? If so, what does the WMP require? 7. What is the reliability of the current water treatment systems and controls? It is important to understand why we are testing. Water treaters test systems for a number of different reasons. Confirming proper operation of feed and control equipment and pretreatment equipment, such as softeners, is necessary to ensure that chemical and water quality measures are within predetermined control parameters. In addition, recording these test results provides valuable data for troubleshooting systems. Some of the parameters that are tested on a regular basis are conductivity, pH, alkalinity, hardness, metals, aerobic bacteria, and chemical inhibitors.
85
the Analyst Volume 27 Number 1
Business Notes continued
Figure 2: Example of a digital titration colorimeter.
“Water in a dynamic system is in a state of constant change.” Open-closed loops. These systems are more dynamic than traditional closed-loop systems described above. Open loops are set up like closed loops, with one major exception—they typically have a tank that is open to the atmosphere. As a result, these systems experience water losses and microbiological growth issues similar to those found in cooling tower systems. This creates the same challenges and complications encountered in cooling towers.
System Types
The type of system often plays a large role in answering the question of testing frequency. Water in a dynamic system is in a state of constant change, meaning that the system’s water is constantly being lost and new water is being introduced to replace it. Other systems are more static in nature; water in a static system is lost at a much slower rate, or not at all. The majority of water systems (Figure 3) may be broken down into the following types: Cooling towers, by their very nature, are dynamic. Cooling tower systems evaporate from 50% to 90% of the water introduced into them, based on incoming water quality. All of the water that evaporates must be replaced with fresh water, which introduces more opportunities for complications. These complications are a result of the fact that every time fresh water, commonly called makeup water, is introduced, a chain of events occurs: mechanical valves must open and close, chemicals must be added, and equilibrium within the system must be reestablished. Automated control equipment will not eliminate the need for testing, since this type of equipment may lose calibration or fail. Steam boilers. A facility with steam boilers provides another example of a dynamic system. The environment in a boiler system is a study in extreme stresses. Because of this aspect, water-related issues can arise quickly, especially if pretreatment or blowdown control equipment should fail. Closed loops. Loops that are not losing large or unexpected amounts of water have much more consistent water quality. As a result, these systems usually require less testing.
86
Domestic water systems provide people with hot and cold water for various applications. These systems have direct human contact and, consequently, usually require additional monitoring and action. Process water/odor control. Facilities with process water systems face unique challenges. Process water systems are used to reduce or eliminate contaminants in both water and air. As a result, the system’s characteristics can change on a minute-to-minute basis or even more quickly. These systems can also be subject to governmental regulation and require more monitoring, documentation, and prescribed corrective actions. Wastewater systems include a wide range of characteristics and concerns that vary from one application to the next. Testing and documentation of results tend to be very important with these systems. Accordingly, they require more monitoring. Specialized equipment to be used in pretreatment applications or as part of a manufacturing process usually represents a substantial investment for the owner and must be monitored to maximize efficiency and usable lifespan. A wide variety of systems exist in the water treatment industry. Each provides its own unique challenges. As a result, the amount of monitoring required varies. Generally, water treatment professionals need to consider how much and how quickly each system changes.
the Analyst Volume 27 Number 1
Business Notes continued
Figure 3: Types of water systems that may be found within an industrial or commercial/institutional facility.
Critical Nature of the System
How critical is the system in question to the operation of the facility? If the system in question fails or shuts down unexpectedly, how much will that cost a company? Will that affect other plants or facilities and have a “chain-reaction� effect? One can make an argument that all systems are important to the operation of a facility. However, some systems play a more significant role than others. When a water treatment system is critical to the function of a plant or facility, the system should be monitored and tested frequently. Testing systems regularly allows owners and operators to head off potential issues before they become large issues that cause system failures and unplanned shutdowns. The more crucial the water system, the more frequently it should be tested.
Location
Where is the facility located? Systems within close proximity to residential areas or medical districts carry greater liability as well as visibility. Therefore, to protect themselves from this increased exposure or liability, facilities must monitor and document any and all fluctuations in operations and maintenance.
Staffing
What is the staffing situation at the facility or plant? In today’s working world, many people are asked to do more 87
with less. Many times, it is a physical impossibility to test a system more than once a day or even a few times a week. In addition, many times testing falls to the less experienced staff members who may not necessarily know how to interpret the results and determine which adjustments may be needed. When such staffing issues arise, it is important to work with your water treatment professional to determine the proper amount of testing required within the time allotted. It is also critical to train all staff on the importance of testing and necessary responses. Testing even occasionally may be better than not testing at all.
Regulations, Consultant, or Company Policy
Are you required to test more frequently because of a governmental regulation, a consultant, or company policy? What does the Authority Having Jurisdiction (AHJ) say? Some cities, states, and communities, such as New York City and New York State, require regimented testing of water systems to meet guidelines and regulations (see Table A). Healthcare groups hoping to receive payment from Medicare and Medicaid for patient services are required to have water risk management plans. Companies may also have specific policies mandating the frequency and types of tests conducted. Additional policies and mandates can also result from oversight of the application by a consultant as well. It is important to know which regulations and policies apply. Your water treatment professional can assist in understanding such requirements. the Analyst Volume 27 Number 1
Business Notes continued
Table A: Example of Water Quality Monitoring Requirements Testing
Short Explanation
Frequency
Water quality parameters, including but not limited to pH, temperature, conductivity, and biocidal indicators, must be measured and recorded as specified in the management program and plan.
Manual measurements
At least three times each week, provided that no more than two days pass without such measurement when the cooling tower system is operating.
Automated measurements (continuous)
When continuous, automated, and/or remote measurements and recordings are used, the management program and plan must show how effective measurements of system process control are being monitored. Automated measurements must be properly recorded and results made immediately available to responsible and qualified persons and to department inspectors when requested.
Note: Information in table is based on New York City Department of Health and Mental Hygiene, Chapter 8-05, Water Treatment, sub (4) (F).
Water Risk Management Plan
Is the plant or facility concerned about Legionella? Do they have a water risk management plan in place that must be followed? Under the correct environmental conditions, a water system could become a source for Legionella bacteria. Legionella is a bacteria that occurs in nature and is common in lakes, ponds, and rivers; however, outbreaks of Legionnaires’ disease rarely originate from these sources. Outbreaks of the illness often occur from exposure to Legionella growing in purpose-built systems such as cooling towers, hot and cold water systems, and spa pools. Water in these systems is maintained at a temperature high enough to encourage growth. Humidifiers, air washers, emergency showers, and ornamental fountains also pose a risk for amplifying Legionella bacteria growth. A water risk management plan will address these causes and help to properly manage, monitor, control, and disinfect systems to comply with the standard.
controls and upstream impacts need to be upgraded and addressed. Testing pieces of pretreatment equipment, such as a softener (Figure 4), helps to diagnose potential issues with its operation. If a softener is passing hard water earlier in its cycle than expected, this can indicate a number of different issues that will need to be addressed. For example, was the brine tank filled with salt to the correct level? Is the flow through the softener too fast, causing “channeling”? After being diagnosed through testing, solutions to issues such as these should be sought out in a systematic manner to ensure efficient operation of equipment. Figure 4: Water softener.
Reliability and Control
Do the pretreatment systems (e.g., softeners, dealkalizers, filters, reverse osmosis) run efficiently with little to no issues? Do the controllers run effectively or do they lose calibration or have other issues regularly? Are water systems being tightly maintained at the edge of control ranges? Is process contamination a concern that would negatively impact a water system? Understanding the limitations of a water treatment system will not only help determine testing frequency but may indicate where
“Are you required to test more frequently because of a governmental regulation, a consultant, or company policy?”
88
the Analyst Volume 27 Number 1
Business Notes continued
Conclusion
There are many reliability, liability, and control factors to consider when determining the proper testing frequency for a plant or facility. While it is impossible to predict when every issue will arise in your system, there are steps you can take to help minimize the impact of these issues. Frequent testing, regularly scheduled cleanings, and proper storage and lay-up can all help to significantly reduce the potential for problems in your facility’s important water systems. Tim Daniels is a corporate engineer at Chem-Aqua, Inc. with a degree from the University of Wisconsin at Whitewater. He has 13 years of water treatment experience and manages Chem-Aqua’s testing line as well as supports a number of specific industries. Among these industries are food, rendering, odor control, and wood products. He resides in Texas with his wife and two young boys. He can be reached at Tim.Daniels@chemaqua.com.
People crafted solutions since 1976.
Custom Blender. super savvy. Our people blend solutions, not chemicals. We manufacture a broad line of proven products for treating any size of commercial or industrial boiler, cooling water, closed loop, airwasher, or wastewater systems. › Expert Technical Assistance › Biocide Sub-registrations Available › Private Labeling, Product Bulletin and MSDS Services › Water, Deposits and Corrosion Coupon Analysis Services › PTSA Dye Trace Cooling Products
Request a FREE CONSULTATION before your next project
423.698.7777 | BrowneLaboratories.com 89
the Analyst Volume 27 Number 1
Advertising Index 27 AMSA, Inc.
38 North Metal & Chemical Company
69 APTech Group, Inc.
59 Nouryon Surface Chemistry (previously Akzo Nobel)
35 Brenntag North America
2
89 Browne Laboratories, Inc.
71 QualiChem, Inc.
80 Chem-Met Company
33 Sanipur US LLC
13 Environmental Safety Technologies, Inc.
51 Scranton Associates, Inc.
15 IDEXX
92 Special Pathogens Laboratory
90 LMI/Milton Roy
81 Walchem, IWAKI America Inc.
57 Lovibond Tintometer
91 Water Science Technologies
Pulsafeeder, Inc.
46 Myron L Company
THE WATER TREATMENT PUMP YOU’VE BEEN WAITING FOR... Introducing LMI’s PD Series Chemical Metering Pump Designed specifically for industrial water treatment applications, the PD Series pump adds advanced technology to fit seamlessly into your process.
2 YEAR WARRANTY Available in two models, Manual and Enhanced, the PD Series sets the industry standard for reliability, convenience, and value.
The wait is over. Contact your local stocking distributor today. www.lmipumps.com • www.RelyOnLMI.com
90
the Analyst Volume 27 Number 1
STOP TREATING THE WATER
by
ONE CHEMISTRY · ONE PRODUCT · ONE SOLUTION
START
PROTECTING THE SURFACE!
WST BIRMINGHAM HEADQUARTERS
1701 Vanderbilt Road, Birmingham, AL 35234 866.284.9244 ∙ info@wstsp.com ∙ www.wstsp.com
Water Safety & Management At Your Fingertips LegiDoc takes the headache out of developing water safety and management plans. The Legionella Experts® in microbiology, engineering, and ASHRAE wrote most of the plan so all you need to do is enter your data. LegiDoc does the rest!
877.775.7284 www.SpecialPathogensLab.com
Fast, easy and affordable No Legionella or ASHRAE expertise required ASHRAE and CMS compliant Professional, high-quality plans in PDF format Backed by Special Pathogens Laboratory
THE LEGIONELLA EXPERTS ®