www.canplastics.com
FEBRUARY 2023
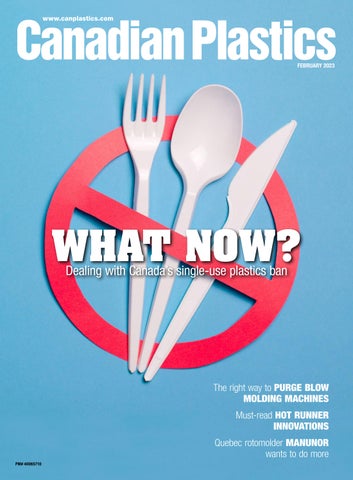
WHAT NOW? Dealing with Canada’s single-use plastics ban
The right way to PURGE BLOW MOLDING MACHINES Must-read HOT RUNNER INNOVATIONS Quebec rotomolder MANUNOR wants to do more PM# 40065710
Shini Granulators Sale - Beside-the-Press Granulators IMS Part #150659 Original: $5,995 Reduced: $4,509
IMS Part #149562 Original: $4,880 Reduced: $3,663
Top feed hopper Sound-proof material hopper
Obstruction alarm Clamshell cutting chamber
• Emergency stop
• Casters included
• Reversible screen
• Low energy consumption
• No specialty tools required for maintenance
• Main power disconnect
Supplies Limited - Call for Availability!
Screenless Granulators
Also Available:
NOT part of the Sale
Features • Top-Feed hopper • Screenless Low Dust / Low Noise Design • Auto Reverse prevents blockage • Heavy Duty Gear Motor • Transparent Polycarb Hopper • 1½" Material Take-off Port • Casters Standard
Staggered Blade Central Granulators High Capacity For Medium To Large Parts*
and Open Rotor Central Granulators High Capacity Granulator For Large Parts* *Not Part of the Sale
Sale! Mold Release Mold Temperature Gate Cutters & Mold Care Control Full Line of Standard, Economy 20% Off List Price.
& Special Application Cutters to Fit All Your Needs!
Maintain Accurate and Consistent Operating Temperature
Purging Solutions Cut the time and cost of color and material changes
Call or Visit Our Websit Today: 800.537.5375 • www.imscompany.com
contents FEBRUARY 2023 VOLUME 82 • NUMBER 1
FROM THE ARCHIVES
The March 1960 issue of Canadian Plastics reported on chemical maker DuPont’s planned construction of a demonstration plant in Maitland, Ont., for the recycling of nylon 6 and nylon 6/6 carpets, as well as other postconsumer nylon waste. The unit, which would be a scale-up of a pilot plant in Kingston, Ont., would transform the nylon waste into hexamethylenediamine, adiponitrile, and caprolactam. The goal of the plant, DuPont said, was to prove that the quality of the recycled product was equivalent to virgin nylon, thereby showing that closed-loop recycling of nylon carpet was doable given the proper infrastructure for collection and the right products.
10 6
Number of the month:
100*
18
* The number of cycles in a household dishwasher that single-use plastic cutlery and straws must survive to avoid being banned in Canada. (See pg. 10)
cover story
10 SINGLE-USE PLASTICS BAN: What now? 4
Editor’s View: Facing the facts about plastic recycling
5
Ideas & Innovations: Implantable polymer ‘sponge’ helps kill cancers
6
News: • Polykar expands into Western Canada with new Edmonton plant • ABC adds injection molding, tooling with WMGT acquisition • Nova reaches mechanical completion of Ontario projects • Supplier News and People
Canada’s single-use plastics ban has begun to take effect. Here’s what it does and doesn’t mean for our industry.
features
14 PURGING: It’s time for a proper blow molding machine purge
Blow molding is the one process that’s been slow to embrace purging. But that’s changing lately, since purging options for blow molders have come a long way.
18 ROTATIONAL MOLDING: Manunor wants to do more
Even as it marks 30 years in business, this Sherbrooke, Que.-based rotational molder is all about looking ahead.
20 Technology Showcase: Focus on hot runners 21 Advertising Index 22 Technical Tips: The fundamentals of press shutdown
Visit us at www.canplastics.com February 2023 Canadian Plastics
3
Canadian Plastics magazine reports on and interprets developments in plastics markets and technologies worldwide for plastics processors, moldmakers and end-users based in Canada.
editor’s view
Facing the facts about plastic recycling
O
ne of the nice things about going to in-person events again is the opportunity for small talk with other attendees. And a topic that seems to come up a lot lately is the acknowledgement that recycling isn’t the magic solution for plastic waste management that many had hoped. Indeed, there seems to have been a sea change – suddenly it’s acceptable to say out loud that recycling plastic is impractical. If I had to guess, I’d say the turning point was a widely publicized Greenpeace report issued late last year that called plastic recycling “a dead-end street.” The Greenpeace report summed the situation up as follows: “Mechanical and chemical recycling of plastic waste has largely failed and will always fail because plastic waste is: (1) extremely difficult to collect, (2) virtually impossible to sort for recycling, (3) environmentally harmful to reprocess, (4) often made of and contaminated by toxic materials, and (5) not economical to recycle.” Let’s acknowledge, first of all, the many impressive technologies developed over the years to improve recycling sortation, and the hard work and resources that went into them. And recycling has benefits, for sure: Recycling paper or cardboard does save trees, and recycling aluminum does save energy. But the reality is that many “recyclables” sent to recycling plants are never recycled, including plastic; and the Greenpeace report supports new figures from the Environmental Protection Agency (EPA) in the U.S. that show the benefits of recycling are relatively small and come almost entirely from recycling paper products and metals, not plastic. So, when even Greenpeace and the EPA admit it, it’s time to acknowledge the fatal flaw that most plastic simply can’t be effectively recycled. Which means it’s also time to pay
4 Canadian Plastics February 2023
more attention to the alternatives of landfilling and incineration. The former gets a bad rap – people think landfills are horrible polluters, but that’s not true. In general, modern landfills are tightly regulated, highly engineered disposal facilities, with protective barriers that don’t leak and landfill gas recovery systems. And eventually landfills are turned into good things: ski hills, parks, and golf courses. Nor, contrary to popular belief, are we running out of space for landfills. All told, for example, North America has about 70 years of landfill capacity remaining in its current facilities – and that’s probably an underestimate, as some landfills add liquids that hasten the decomposition process and add more time to the life of the landfill. As for incineration, burning plastic trash to create energy sounds sensible: plastic is, after all, made from hydrocarbons, just like oil, and is more energydense than coal. Sophisticated incinerators that burn plastic and other waste can produce enough heat and steam to turn turbine blades and generate electricity for the local grid, and are also fitted with devices that capture air pollutants and emissions. The European Union, for example, which restricts the landfilling of organic waste, already burns almost 42 per cent of its waste. Another benefit is that incineration provides an option for cities with little land available for landfills. A particularly attractive technology right now is pyrolysis, in which plastics are shredded and melted at lower temperatures than gasification. The heat breaks plastic polymers down into smaller hydrocarbons, which can be refined to diesel fuel and even into other petrochemical products – including new plastics. To modify the famous line from The Graduate, then, the future of plastic recycling is probably three words: landfilling and incineration.
www.canplastics.com Reader Service Print and digital subscription inquiries or changes, please contact Angelita Potal Tel: 416-510-5113 Fax: 416-510-6875 email: apotal@annexbusinessmedia.com Mail: 111 Gordon Baker Rd., Suite 400 Toronto, ON M2H 3R1 EDITOR Mark Stephen 416-510-5110 Fax: 416-442-2230 mstephen@canplastics.com ASSOCIATE PUBLISHER Stephen Kranabetter C: 416-561-5362 W: 416-510-6791 skranabetter@annexbusinessmedia.com MEDIA DESIGNER Lisa Zambri lzambri@annexbusinessmedia.com ACCOUNT COORDINATOR Cheryl Fisher 416-510-5194 cfisher@annexbusinessmedia.com AUDIENCE DEVELOPMENT MANAGER Serina Dingeldein 416-510-5124 sdingeldein@annexbusinessmedia.com GROUP PUBLISHER/VP SALES Martin McAnulty mmcanulty@annexbusinessmedia.com PRESIDENT/COO Scott Jamieson sjamieson@annexbusinessmedia.com PRINTED IN CANADA ISSN 008-4778 (Print) ISSN 1923-3671 (Online) Publication Mail Agreement #40065710 2023 SUBSCRIPTION RATES 5 issues Canadian Plastics, plus Dec. 2023 Buyers’ Guide: CANADA: 1 Year $77.50 plus applicable taxes; 2 Years $123.50+ taxes USA: $176.00 (CAD) / year FOREIGN: $201.00 (CAD) / year
Occasionally, Canadian Plastics will mail information on behalf of industry related groups whose products and services we believe could be of interest to you. If you prefer not to receive this information, please contact our audience development department in any of the four ways listed above. Annex Privacy Officer privacy@annexbusinessmedia.com • Tel: 800-668-2374 No part of the editorial content of this publication can be reprinted without the publisher’s written permission ©2023 Annex Business Media. All rights reserved. Opinions expressed in this magazine are not necessarily those of the editor or the publisher. No liability is assumed for errors or omissions. All advertising is subject to the publisher’s approval. Such approval does not imply any endorsement of the products or services advertised. Publisher reserves the right to refuse advertising that does not meet the standards of the publication. MEMBER: Magazines Canada, Canadian Plastics Industry Association.
Mark Stephen, editor
mstephen@canplastics.com www.canplastics.com
ideas & innovations
Implantable polymer ‘sponge’ helps kill cancers
Image Credit: Negin Majedi/Symphony Biosciences
A
n interdisciplinary research team at the University of California, Los Angeles (UCLA) has developed a therapeutic sponge the size of a pencil eraser that’s been shown to boost the body’s tumor-fighting response in mice and keep the cancer from returning. Called a SymphNode, the implantable biodegradable device is made from alginate, the same jiggly polymer used to thicken pudding, and works by keeping in check the extra white blood cells known as regulatory T cells, or Treg cells, that surround the tumor. Treg cells protect the tumor but they also play a critical role in safeguarding healthy tissues. Attempting to treat cancer by deactivating Treg cells can have serious consequences throughout the body by causing auto-immune conditions. When surgically implanted directly next to a tumor, the sponge stimulates the body’s immune response against cancer by slowly releasing a drug that blocks the regulatory Treg cells in the tumor, while at the same time attracting and beefing up the Treg cells that kill tumors. The material that the device is made of resembles a lymph node, a welcoming setting for cancer-fighting cells, and has pores lined with antibodies that further activate those cells. “Getting rid of regulatory T cells within the tumor seems to be transformative,” said UCLA team member Manish Butte. “Every solid tumor is crammed with these cells, and they’re why 91 per cent of cancer deaths occur from solid tumors. They’re probably limiting our ability to cure the cancer in the first place.” The UCLA team tested the SymphNode in mouse models of both breast cancer and melanoma. With breast cancer, the device shrank tumors in 80 per cent of mice and prevented the spread of cancer in 100 per cent of them; the researchers also found that placing a SymphNode next to one breast cancer tumor halted the growth of a second tumor at a different location in the body. In melanoma, the device shrank tumors in 100 per cent of treated mice, with tumors decreasing to undetectable levels in more than 40 per cent of cases. In both types of cancer, the treatment significantly extended the life span of mice, in many cases by more than twice that of untreated mice. Most promising, the research showed that mice whose breast cancer was treated with a SymphNode and survived also resisted the growth of a second tumor injected 100 days after the first, indicating that the technology may decrease the risk of cancer returning. The UCLA team has licensed its technology to cancer drug developer Symphony Biosciences, which is headquartered on the UCLA campus. Symphony is currently developing a smaller, injectable version of the SymphNode, which could be used as a potential addition to chemotherapy or other first-step cancer treatments; and the company hopes to initially apply the technology to triple-negative breast cancer, an aggressive form of the disease that lacks targeted CPL therapies. Clinical trials could begin next year.
The SymphNode device (left), contains nanoparticles (red dots) that release a drug that blocks the activity of regulatory T cells (green), which suppress the body’s response to solid tumors. At the same time, the SymphNode’s microparticles (black dots) attract and beef up cancer-fighting T cells.
PURGING PERFECTION What does purging perfection look like? Industry leadership, decades of innovation, outstanding customer service, technical expertise and product that’s effective every time. When your work has to be perfect, trust the leader. Trust Dyna-Purge. Request a free sample of Dyna-Purge and see for yourself. Discover the Difference. 866-607-8743 www.dynapurge.com DYNAPURGE is a registered trademark of Shuman Plastics, Inc. February 2023 Canadian Plastics
CP_PurgingPerfection_Resized.indd 1 CPL_ShumanPlastics-Dyna Purg_JanFeb23_CSA.indd 1
5
2017-02-23 7:27 9:19 AM AM 2023-01-27
news
Polykar expands into Western Canada with new Edmonton plant
key contributor to our future growth plans,” company officials said. Founded in 1987, Polykar makes film converted by other companies as well as its own finished goods, including garbage bags, industrial packaging, and food packaging. Polykar also sells recycled resins to other manufacturers. CPL
ABC adds injection molding, tooling with WMGT acquisition
Malpack to be acquired by Sweden’s Trioworld Group
T
P
oronto-based automotive parts supplier ABC Technologies Holdings Inc. is adding more expertise in both injection molding and tooling with its acquisition of Windsor Mold Group Technologies (WMGT) for US$165 million. WMGT, based in Windsor, Ont., is a Tier 1 and Tier 2 supplier to the auto industry and a maker of complex tooling for injection molded exterior and interior parts, lighting molds, and optic inserts, ABC officials said in a December 2022 news release. It saw US$270 million in sales for its fiscal year that ended April 30. WMGT has operations in Windsor; Amherstburg, Ont.; Saline, Mich.; Bellevue, Ohio; Pulaski, Tenn.; Pharr, Tex.; and Querétaro, Mexico. The acquisition was the third of 2022 for ABC and adds to its capabilities as a vertically integrated supplier. “This acquisition strengthens our exterior products offering, expands our injection molding technical expertise, and brings additional value-added tooling in-house,” ABC president and CEO Terry Campbell said in the release. WMGT has been owned by the Biere family. Its sale to ABC marks the “next phase of [its] journey,” WMGT president and CEO David Mastronardi said in the release. “I’m confident that the combination of our businesses — enabled by a continued focus on people, quality, and customers — will catalyze meaningful growth and opportunities while establishing the combination as a supplier of choice.” The acquisition is expected to close in early 2023. CPL
6 Canadian Plastics February 2023
lastic packaging supplier Trioworld Group is extending its stretch film manufacturing capabilities to North America through the pending acquisition of Ontariobased Malpack. Trioworld, based in Smålandsstenar, Sweden, has an agreement to purchase both Malpack Ltd. of Canada and Malpack Corp. in the U.S., makers of stretch film for the transit packaging segment. “We see Trioworld as a uniquely positioned strategic sponsor and partner that will help us to accelerate plans to take our North American business to the next level,” Malpack chief operating officer Ricardo Cardoso said in a December 2022 news release. As a result of the deal, Cardoso will become Malpack’s CEO and the new Trioworld North America division president. Malpack is headquartered in Ajax, Ont., where the company produces stretch films for the distribution, beverage, food, consumer goods, electronic, and industrial segments. The company, with 260 workers, also has a network of distribution centres in North America, Trioworld said. “With our joint forces, we’ve now established a strong foothold in the Canadian and U.S. markets and will continue to ambitiously develop our joint offering,” Trioworld CEO Andreas Malmberg said in the release. Malpack began operations in 1972 as a plastic bag maker and started producing films in 1997. CPL www.canplastics.com
Photo Credit: Polykar Inc.
S
aint-Laurent, Que.-based plastic film maker and recycler Polykar Inc. has opened a new 50,000-square-foot plant in Edmonton that will serve customers in Western Canada as well as parts of the U.S. “This puts Edmonton squarely at the forefront in terms of creating value-added products from the raw materials made in Alberta,” Polykar CEO Amir Karim said in a December 2022 statement. “It includes a cutting-edge recycling facility, positioning [us] to actively participate in Alberta’s efforts to divert plastic waste from landfills.” The new Polykar site created 50 new jobs, and the company expects to add another 20 workers in the next two years. The Edmonton facility becomes Polykar’s second plant in Canada, joining the company’s existing location in SaintLaurent. The company broke ground for the new location in July 2021, and also announced that it has purchased an additional 1.5 acres of land just north of the plant for future development. “[This] underscores [our] confidence in Edmonton as a
Nova reaches mechanical completion of Ontario projects
C
Photo Credit: Nova Chemicals Corp.
algary-based material supplier Nova Chemicals Corp. has reached mechanical completion on its second Advanced Sclairtech technology (AST2) facility and on the third phase of its Corunna cracker expansion project in Ontario. In a December 2022 news release, Nova officials said that the world-scale AST2 facility, which is located at the new Rokeby site in St. Clair Township, Ont., will have a produc-
tion capacity of approximately one billion pounds of polyethylene (PE) per year. The cracker expansion will provide ethylene feedstock to the new AST2 facility, the release continued, expanding the existing cracker’s current capacity by more than 50 per cent. Both projects represent what Nova calls “a significant investment,” bringing new technology, jobs, and long-term economic viability to the region. Since the growth projects began in late 2017, Nova said, they’ve added approximately $2 billion to the provincial economy and employed over 7,000 workers. Nova also estimates that 150 permanent full-time jobs will be added at both facilities once the projects are fully commissioned and complete. Post-construction commissioning activities at the Rokeby site are fully underway, Nova said. Nova’s Corunna site produces 1.8 billion pounds of ethylene and approximately 700 million pounds of coproducts annually. Corunna provides feedstock to Nova’s Moore and St. Clair River sites, where they convert ethylene into up to 1.3 billion pounds of PE per year. Ethane is the primary feedstock for ethylene production at the Corunna site. CPL
Fiberglass Cooling Towers are Economical & Built to Last
Advantage Engineering’s Newest Non-rusting Fiberglass Evaporative Cooling Towers provide one of the lowest costs of cooling per ton compared with other cooling systems such as chillers & fluid coolers. Cooling towers and systems by Advantage Engineering are economical, easy to install and simple to operate. • 45 – 270 ton cooling capacity • • All fiberglass construction for long life • • Low maintenance direct drive fan • • 10 year shell & 5 year mechanical warranty •
525 East Stop 18 Road Greenwood IN USA
317-887-0729
Chillers Inc of Newmarket Ontario is the exclusive representative of Advantage products in Canada.
Learn more
Solely focused on process water cooling systems February 2023 Canadian Plastics CPL_Chillers_Nov22.indd 1
7
2022-10-31 3:11 PM
news
SUPPLIER NEWS
Medline Canada buys Stat Healthcare
– Processing machinery and auxiliary equipment supplier Plastics Machinery Inc. (PMI), of Newmarket, Ont., has been appointed as the Canadian representative for Routsis Training Inc. Dracut, Mass.-based Routsis offers both in-person and online certification programs for training in injection molding, extrusion, and extrusion blow molding.
M
edical products maker Medline Canada Corp. has acquired Calgary-based Stat Healthcare Corp., a medical and laboratory supplies provider with expertise in clinic set-ups. The financial terms of the deal have not been disclosed. In a Jan. 11 news release, officials with Mississauga, Ont.based Medline said the deal will grow its medical supplies market share across the continuum of care – acute, long-term, and primary – in Canada. Stat Healthcare will operate as a division of Medline Canada, providing supplies for the medical, surgical, homecare, veterinary, anesthesia/respirator, and laboratory supply fields, as well as offering specialties in medical clinic set-ups and surgical suite accreditation. Medline now has eight distribution centres across Canada, including a national distribution hub in Guelph, Ont. CPL
– Maguire Canada, of Vaughan, Ont., has appointed Mascouche, Que.-based agency Industries Laferrière as its new sales representative for Quebec and the Maritime provinces, handling the complete range of auxiliary equipment products – including blenders, dryers, loading systems, auger feeders, granulators, material conveying systems, and outdoor resin storage silos – offered by Maguire Products Inc., Novatec Inc., and Dri-Air Industries.
PEOPLE
Joe Herres
Thorsten Dreier
Samir Hifri
Anthony Toklo
Wendy Herbst
Beatrix Praeceptor
Li Yong
Alexandra Coffey
Peter Gardner
Paul Caprio
John Wiley
Marc Fern
Monica Christler
Michael Foldvary
Remo Heusi
Ib Jensen
Hans Werhonig
Levi Kishbaugh
– Additives supplier Chroma Color Corp., headquartered in McHenry, Ill., has named Joe Herres as vice president of sales and marketing. – German materials company Covestro AG has named Thorsten Dreier as chief technology officer; and Samir Hifri as chairman and president of Covestro LLC, its U.S. operations. – Pawcatuck, Conn.-based extrusion technology maker Davis-Standard LLC has appointed Anthony Toklo as chief marketing officer. – Westlake, Ohio-based material supplier Geon Performance Solutions has named Wendy Herbst as chief commercial officer. – Austria-based Greiner Packaging International GmbH has named Beatrix Praeceptor as CEO. – German plastics machinery maker KraussMaffei Group has named Li Yong as CEO and management board chairman, and Alexandra Coffey as senior sustainability manager.
8 Canadian Plastics February 2023
– Duluth, Ga.-based injection molding machine maker LS Mtron Injection Molding Machines USA has named Peter Gardner as president, Paul Caprio as president of sales, and John Wiley as business development manager. – Northbrook, Ill.-based resin distributor M. Holland Co. has named Marc Fern as president and chief operating officer; Monica Christler as executive vice president, commercial; and Michael Foldvary as vice president, distribution. – Swiss injection molding machine maker Netstal has appointed Remo Heusi as vice president of global service. – Sweden-based specialty chemical maker Perstorp Group has named Ib Jensen as CEO. – South Korea-based chemicals and additives maker Songwon Industrial Co. Ltd. has named Hans Werhonig as leader group commercial. – Wilmington, Mass.-based foaming technology supplier Trexel Inc. has named Levi Kishbaugh as CEO.
www.canplastics.com
Molded to Perfection Molded to Perfection
MoldedMolded to Perfection to Perfection Molded to Perfection With over 160 years of steel production experience backing Steel Group is not only a pioneer, but also a market leader in Molded to Perfection With over 160 years of steel production experience backing their brands, Swiss backing Their comprehensive Formadur®, Thermodur®, Cr With over 160 years ofrange steelof production experience Steel Group is not only a pioneer, also is aallows market leader in specialty steels. Die® grades you choose thealso ideally suitedleader mold m Steelbut Group not only ato pioneer, but a market in Molded to Perfection Molded to Perfection Their comprehensive Formadur®, Thermodur®, Cryodur®, Mold cation. In addition, anrange extensive range ofand value added service With over 160 years ofrange steelof production experience backing their brands, Swiss Their comprehensive of Formadur®, Thermodur®, Cr Die® grades allows you to choose the ideally suited mold material for your applimore alternatives from one source, Swiss Steel USA / Canad Steel Group is not only a pioneer, also aallows market leader in specialty steels. Die®but grades you to choose the ideally suited mold m Molded to Perfection cation. In addition, anrange extensive range value added services provides you with Their comprehensive ofWith Formadur®, Thermodur®, Cryodur®, Mold cation. Inof addition, anofextensive range ofand value added service over 160 years steel production experience backing With over 160 years of steel production experience backing their brands, Swiss Steel Group is not only a pioneer, but also a market leader in specialty steels.
Their comprehensive range of Formadur®, Thermodur®, Cryodur®, and Mold With 160allows years you of steel production experience their brands, Die®over grades to choose the ideally suitedbacking mold material for yourSwiss appliSteel Group is not only a pioneer,range but also a market leader in specialty cation. In addition, an extensive of value added services providessteels. you with Their comprehensive range of Formadur®, Thermodur®, Cryodur®, and Mold more alternatives from one source, Swiss Steel USA / Canada.
Die® grades allows you to choose the ideally suited mold material for your appli-
cation. In addition, an extensive range of value added services provides you with www.swisssteel-international.us more alternatives from one source, Swiss Steel USA / Canada. www.swisssteel-international.ca With over 160 years of steel production experience backing their brands, Swiss +1 800 323 1233 Steel Group is not only a pioneer, but also a market leader in specialty steels. www.swisssteel-international.us more alternatives from one source, Swiss Steel USA Their comprehensive range of Formadur®, Thermodur®, Cryodur®, and Mold www.swisssteel-international.us Die® grades allows you to choose the ideally suited mold material for your applimore alternatives from one source, Swiss Steel USAleader / Canad Steel Group is not only a/ Canada. pioneer, but also a market in www.swisssteel-international.ca Die® grades allows you to choose the ideally suited mold material for your appliwww.swisssteel-international.ca cation. In addition, range ofexperience value added services provides you with +1 an 800 323 1233 With over 160 years ofextensive production backing their brands, Swiss Their comprehensive Formadur®, Thermodur®, Cr cation. Insteel addition, an extensive range of valuerange added of services provides you with
www.swisssteelgroup.com +1 800 323 more Group alternatives from one source, Swiss Steel USA / to Canada. alternatives from one source, Swiss Steel USA / Canada. www.swisssteel-international.us Steel is notmore only a pioneer, but also1233 aallows market leader in specialty steels. Die® grades you choose the ideally suited mold m +1 800 323 1233 www.swisssteel-international.ca Their comprehensive range ofcation. Formadur®, Thermodur®, Cryodur®, Mold In addition, an extensive range ofand value added service www.swisssteel-international.us
www.swisssteelgroup.com +1 800 323 1233 Die® grades allows you to choose the ideally suited materialSwiss for your applimore alternatives from mold one source, Steel USA / Canad www.swisssteel-international.ca +1 800 In 323 1233+1 an cation. addition, 800extensive 323 1233 range of value added services provides you with more alternatives from one source, Swiss Steel USA / Canada. www.swisssteel-international.us www.swisssteel-international.ca www.swisssteelgroup.com +1 800 323 1233 +1 800 323 1233
cover story
Dec. 20, 2025. A prohibition on the manufacture and import for sale in Canada of ring carriers or six-pack rings, used to carry aluminum cans and plastic bottles, will begin on June 20, 2023; their sale will be banned by June 20, 2024; and their manufacture, import, and sale for export will be prohibited starting Dec. 20, 2025.
WHAT NOW? Canada’s single-use plastics ban has begun to take effect. Here’s what it does and doesn’t mean for our industry. By Mark Stephen, editor
F
or almost anyone alive nearly a century ago, Oct. 24, 1929 was a date to be remembered for its economic consequences: the stock market crash that triggered the Great Depression. Fast forward to today, and another date has just passed that might be almost as economically important for Canada’s plastics sector: Dec. 20, 2023, which is when the national ban on single-use plastics began to take effect. Devised by the federal government to help reach its goal, set in 2018, of zero plastic waste by 2030, the ban covers six single-use plastic products: checkout
10 Canadian Plastics February 2023
bags, cutlery, foodservice ware that’s made from “problematic” or hard-torecycle materials, ring carriers, stir sticks, and straws. The manufacture and import for sale ban in Canada is the first step. Consumers will slowly see the phase-out of these products over the next year to “allow businesses in Canada enough time to transition and to deplete their existing stocks,” according to the government’s website. While the ban on the sale of these products began on Dec. 20, a prohibition on the manufacture, import, and sale for export of these plastics is due to take effect on
Photo Credit: Adobe Stock/ julie208
GOING THROUGH THE LOOPHOLES
At first glance, the ban appears total, but it’s not quite that. As with most government actions, it’s complex and – fortunately for some of the processors in our industry – riddled with exemptions. While checkout bags made entirely or in part from plastic and used to carry purchased goods from a business will be banned, plastic bags that are used to hold organic waste – including pet waste – garbage, and recycled items aren’t prohibited, and neither are plastic bags used to package fruit and vegetables, meat, flowers or potted plants, clothing, baked goods, and loose bulk food items such as candy and nuts. (The ban also includes fabric bags that don’t pass a stress test, meaning they can’t break or tear if carrying 10 kilograms over a distance of 53 metres, 100 times, or when washed.) For single-use cutlery, meanwhile, the ban applies to forks, knives, spoons, sporks or chopsticks that contain polystyrene (PS) or polyethylene (PE), or plastic items that change their physical properties after being run through a dishwasher 100 times, but not to reusable plastic cutlery made from material other than PS or PE and that can withstand being washed in a dishwasher 100 times. Food containers and cups that are made entirely or in part from plastic are banned, as well as those that contain expanded or extruded PS, the latter commonly referred to as Styrofoam; polyvinyl chloride (PVC), often used in salad containers; carbon black or black plastic food containers that usually come with a transparent lid; and oxodegradable plastic. Canadians will also not be able to buy single-use plastic www.canplastics.com
cover story
cups, plates, and bowls after the prohibition on sale comes into force in December 2023. But other products are allowed: plastic trays used for storing raw meat, fish, and vegetables wrapped in plastic film, and pre-cooked food packaged in flexible plastic packaging; cups or containers used by hospitals and care institutions for providing medication to patients; paper- and fibre-based coffee cups with a plastic lining that don’t contain prohibited plastic; foodservice wares made from non-prohibited kinds of recyclable plastic, or nonconventional or compostable plastic; and containers used for the long-term storage of food such as peanut butter, apple sauce, olives or nuts. The manufacture and import of single-use plastic ring carriers that are designed to surround beverage containers to carry them together – typically made from low-density PE (LDPE) – will be banned in June 2023, but rigid plastic beverage holders aren’t prohibited because they don’t have deformable rings or bands surrounding the beverage container. Finally, all types of plastic stir sticks are banned, period, and so too are plastic drinking straws that contain PS or PE, that can’t withstand going through the dishwasher 100 times, and that are attached to or sold with juice boxes, bags or pouches. But the manufacture and import of single-use plastic flexible straws not packaged with a beverage container are excluded under certain
conditions, such as to accommodate people with disabilities; and hospitals, medical facilities, and other care institutions are allowed to offer plastic flexible straws to their patients and residents. For retailers, meanwhile, selling plastic flexible straws just got complicated: they’re required to keep plastic flexible straws out of view, but can sell a package of 20 or more single-use plastic flexible straws if a customer asks for it.
PUSHING BACK
Exemptions notwithstanding, the ban is probably opposed by most – if not everyone – in the Canadian plastics industry, and resistance to it began almost as soon as it was announced. The Chemistry Industry Association of Canada (CIAC) filed a Notice of Objection to the ban in February 2022, and so too did a number of Canadian plastic bag makers. And in August 2022, the Responsible Plastic Use Coalition (RPUC), consisting of more than two dozen North American plastics companies including some of the largest resin makers and processors, sued to block the ban. (In June 2021, RPUC filed a lawsuit that sought to overturn the government’s decision to designate plastics as “toxic” under the Canadian Environmental Protection Act.) “The ban was made despite a paucity of facts and evidentiary support about the nature and extent of the environmental contamination and harm arising from single-use plastics,” RPUC said in August 2022.
“Accordingly, the ban cannot be justified as an exercise of the criminal law power conferred upon Parliament.” There’s self-interest involved here, of course – not that this is a bad thing, as an untold number of jobs may hinge on continuing to make single-use plastic products. But there’s also the objection, backed up firmly by science, that the ban not only won’t achieve anything concrete, but is actually counterproductive since all replacement materials are worse, by any measure. Take paper bags, for example, which are believed by many to be more environmentally friendly than plastic bags because they’re made from a renewable resource, can biodegrade, and are recyclable. Research shows just the opposite, however: Plastic bags outperform paper bags environmentally – on manufacturing, on reuse, and on solid waste volume and generation. Paper products take substantial amounts of energy to make, making paper and cardboard the third largest industry use of energy on the planet. Compared to cardboard, plastic is lighter, more durable, and less energyintensive to manufacture. The CIAC, and many others, alluded to this when pushing back against the ban. “No evidence [has been provided by a government assessment] that the use of substitutes will reduce littering and pollution in the environment,” CIAC said in its Notice of Objection. “Bans will not address the behaviours causing the environmental leakage. In
Increase uptime Improve operation Enhance product quality
®
February 2023 Canadian Plastics CPL_Davis Standard_JanFeb23_CSA.indd 1
11
2023-01-23 1:37 PM
Photo Credit: Adobe Stock/Satjawat
cover story
Hospitals, medical facilities, and other care institutions are still allowed to offer plastic flexible straws to their patients and residents.
fact, the assessment acknowledges that alternatives to plastic will lead to higher pollution, thus the government is proposing substitutes that will not actually achieve environmental goals.” And a 2022 report by The Fraser Institute, entitled Canada’s Wasteful Plan to Regulate Plastic Waste, reached the same conclusion. “Canada has launched a regulatory campaign against plastic waste...that will have a negative impact on Canada’s overall economic health, the health of Canadian private-sector businesses, Canada’s imports and exports, and Canadian consumer choice (both domestic and international),” the report said. “It could, via substitution effects, lead to increased environmental damages rather than their reduction.” But as an executive at one plastic product maker told Canadian Plastics, what the science says no longer matters. “Unfortunately, there’s little to say about what’s been done because it can’t be undone,” he said.
AHEAD OF THE CURVE
And on the assumption that the ban won’t be undone, some companies moved to eliminate their plastic items early on, before it became mandatory, while others are responding to the ban now. Tim Hortons had already been
12 Canadian Plastics February 2023
using paper straws since October 2020, but on the same day that phase one of the ban came into effect, the company announced that it would be rolling out cutlery made of wood and fibre starting in early 2023. Tim Hortons also plans to introduce a new breakfast and lunch food wrapper the company says uses 75 per cent less material; and in Vancouver, the company is also testing new beverage lids made from fibre. Nor is Tim Horton’s the only coffee company rushing to replace single-use plastic items. Starbucks Canada announced in August 2021 that it was switching to paper straws and cutlery. Starbucks also resumed its bring-your-own-cup program in August 2021 after temporarily putting it on hiatus due to COVID-19 concerns – customers who bring their own cup can also get a 10-cent discount on their drink; and the company is also charging 25 cents for single-use cups at its stores in Vancouver, in compliance with city bylaws. Among restaurant chains, A&W Canada has already made the switch to paper straws – the company announced the phase-out of plastic straws back in 2018 and is also one of the few fast food chains to offer metal baskets, glass mugs, and ceramic plates to dine-in customers. Also in 2018, Subway Canada introduced paper straws, completing its
transition in August 2019. And in October 2021, McDonald’s Canada announced it would be switching to paper straws and wooden cutlery and stir sticks; McDonald’s has also allowed customers to bring their own reusable mugs for coffee and tea orders since July 2022. Among the grocery and retail chains, meanwhile, Sobeys announced its move away from single-use plastic bags back in January 2020, becoming the first national Canadian grocery store to do so. Metro announced in June 2022 that it would stop giving out plastic bags at its stores by September of that year. Loblaw Companies also announced in June plans to eliminate single-use plastic shopping bags by the first quarter of 2023; and in October, the company announced the phase-out had been completed in Manitoba, Saskatchewan, and the Northwest Territories. And in April 2022, Walmart Canada stopped offering plastic bags, switching instead to reusable cloth bags.
DEALING WITH IT
All of which leaves our industry with no alternative but to deal with the ban, at least for the foreseeable future. Which means being flexible enough to adapt to the new playing field. “These new regulations will greatly change the requests of our customers, and the markets will shift to films that can be used in recyclable multi-layers and containing postconsumer recycled materials,” said Pierre Sarazin, vice president of research and development and sustainability with Laval, Que.-based blown film maker PolyExpert Inc. For Brantford, Ont.-based straw and food packaging manufacturer Stone Straw Ltd. – part of the Wentworth Technologies group and sister company Amhil North America – the ban on straws has some immediate effects as well as unknown implications for the longer term. “We got ahead of the straw ban by moving from polypropylene [PP], which our straws were traditionally made from, into compostable biopolymers early on,” said Abe Looy, vice president of operations with Stone Straw and Amhil North America. “We launched our first-generation Back to www.canplastics.com
cover story Earth compostable straws in 2019; and our second-generation Back to Earth straws, made from a cellulose acetate formula derived from wood pulp and vinegar, in 2021.” But Stone Straw’s second-generation line can’t withstand being run through a dishwasher 100 times because they’re meant to break down easily, Looy said, and the firstgeneration straws are still in the process of being tested – which means, ironically, that the company’s original PP straws, which do satisfy the dishwasher regulation, might just be the only straws it can dependably market in Canada. “Obviously, we’re disappointed that our cellulose acetate formula doesn’t meet the government’s regulation for straws, but we plan to use the formula for other Amhil products that aren’t banned, such as cups, lids, and clamshells. Regarding straws, in the short term we’re continuing to make our original PP straws for Canada; we’re waiting on testing on our first-generation Back to Earth straws;
“The ban was made despite a paucity of facts and evidentiary support about the nature and extent of the environmental contamination and harm arising from single-use plastics.” and our second-generation straws are still being produced here and shipped to the U.S., but that will end when the ban on exportation begins in 2025.” And in the longer term, Looy said, Stone Straw is developing a backup plan in case the federal government ever closes the 100-dishwasher-cycle loophole. “If that happens, we intend to move our plastic and compostable straw production to the U.S. – either to an existing Wentworth facility or to a new site, depending on space requirements – and make paper straws for the Canadian market from our current plant in Brantford,” he
said. “That’s a last resort – we’d prefer to stay in Canada, and we’ll remain in contact with the government going forward to see if there’s ever a plan to close that loophole.” And while the odds might not be high, there’s always the chance the ban could be either revoked or revised under a new federal government, or struck down by a court. “There’s a recent example of this in France, where a ban on plastic packaging around certain fruits and vegetables went further than the law allowed and was struck down,” said Pierre Sarazin, who has written extensively online about Canada’s plastics ban. “Bans can be difficult to keep in place if scientific studies show there’s no positive impact to them on the environment.” But one thing seems clear: Regardless of whether the single-use plastics ban remains in place for good or is eventually overturned, Dec. 20, 2022 is a date our industry won’t soon forget. CPL
CREATE FORMULATIONS THAT GO BEYOND EXPECTATIONS When you’re looking for a customizable solution that enhances physical properties without compromising performance, Honeywell’s range of performance additives deliver on point. From lubricity to productivity to better filler and pigment dispersion, enhance a range of properties of your plastic formulations with Honeywell’s customizable high-performance additives offering. Let’s develop a solution that’s ideal for you. Contact our experts today!
LEARN MORE
Proudly distributed by CCC Plastics
February 2023 Canadian Plastics CPL_CCC_Nov22.indd 1
13
2022-10-27 3:44 PM
IT’S TIME FOR A PROPER
BLOW MOLDING MACHINE PURGE Blow molding is the one process that’s been slow to embrace purging. But that’s changing lately, since purging options for blow molders have come a long way. By Mark Stephen, editor
B
low molding is the main molding method for producing hollow products, but there’s nothing hollow about the process itself. It’s complex, and according to different manufacturing methods, it can be divided into the three main methods of extrusion blow molding, injection blow molding, and stretch blow molding, each differentiated by the types of products they create and materials they process. What all three have in common, however, is the need for regular purging of the machines in order to prevent layers of carbon from building up, reduce the potential of cross-contamination of resins or colours, and lessen or eliminate the need to pull the screw out for cleaning. But, as far as purging goes, that’s where the similarity ends: For each of the three main methods, there are different purging steps required. And, in a bad way, it wasn’t always like this. Blow molding is the one process that’s been slow to embrace purging. For many years, purge suppliers simply didn’t have grades that performed well enough to justify implementing a purge program; and because of this reluctance, many blow molders experienced, and got used to, changeover times between 8 and 24 hours, helped along – sometimes just barely – by using the next processing resin or regrind for a purge. Fortunately, commercial purging compounds (CPCs) have come a long way in recent years, and blow molders now have a range of options.
14 Canadian Plastics February 2023
Purge holding a parison in the head of a blow molding machine.
CHOOSING WISELY
And selecting the right CPC comes before anything else. Making the intelligent decision here requires a bit of work and research – not only are there mechanical, chemical, and chemicalmechanical hybrid types of CPCs now available, but each CPC manufacturer has its own proprietary composition, different from the others. Most of the suppliers now also have specific grades for blow molding, which tend to be chemical, although not always. ChemTrend, for example, recently introduced two new chemical CPCs for blow molding. “Our UltraPurge 3060 is designed for accumulator-head blow molding, and the UltraPurge 3615 is for machines that don’t have an accumulator,” said Andrew
Reeder, Chem-Trend’s sales manager, thermoplastics. Techmer PM, meanwhile, designed its new PFM117632 purging agent specifically to clean out the melt flow channels in extrusion blow molding machines; the compound works on both polyethylene (PE) and polypropylene (PP), the company said, and can withstand a maximum processing temperature of 260°C or 500°F. And Asaclean offers both purging concentrates and chemical CPCs for blow molders, but also recommends mechanical CPCs for certain situations. The key in any situation is to consult with the CPC supplier beforehand to find the right solution for a particular product or process, since the grade of the CPC will depend on the type of plastic used with the blow molding machine and the processing temperature. And while blow molders may still view homemade purge remedies or nextresin purging as less expensive, CPCs – no matter what the price tag – are virtually always more cost-effective in the long run. “It’s the price per purge that matters, not the price per pound,” Reeder said. “In-house resin purging is generally a very slow process, with the purging resin just layering over previous layers of contaminants, and eventually this creates its own cost in downtime. A homemade purge is usually the least cost-efficient method.” Extrusion blow molding heads and accumulators are, by design, low-pressure areas, and this can lead to difficulty cleaning certain areas. Since mechanical purging compounds – which primarily utilize shearing force to remove contaminants from processing surfaces – require maximum pressure, they might not be the best choice for this application. Instead, some suppliers say, try using a chemical CPC, which operates by utilizing heat-activated chemicals to break down bonds between the various contaminants and processing surfaces in a chemical reaction in the barrel or die, and which usually requires between 5 to 30 minutes of “soak” time to deliver an effective purge. “To purge an extrusion blow molding machine, I recommend chemical grades almost exclusively, due to the low-pressure environment www.canplastics.com
Photos courtesy of Asahi Kasei Asaclean Americas
purging
purging
involved with the process,” said Eric Despotovich, technical sales representative with Asahi Kasei Asaclean Americas.
HOW TO DO IT
With extrusion blow mold purging, there are a few general rules. First, it’s not critical to hold a parison while purging – these machines are relatively easy to start back up after purging, and gravity will control the purge after exiting the head tooling. Second, run the die as close to closed as safely possible to increase melt pressure and shear, and keep an eye on extruder amps to make sure the motor isn’t being overworked. And third, consider using the so-called “disco purge” method, which involves changing screw speeds and stopping and starting screw rotation. “These short bursts of high agitation will loosen buildup, and then subsequently slowing the speed of the screw allows the purge to expand and then push out the loosened contamination,” said Bob Grzegorek, global technical services manager with Shuman Plastics, which supplies the Dyna-Purge line. Depending on the resin being processed, Eric Despotovich said, the molder may be able to use a mechanical purge – which most processors already know about as the purge compound favoured by the injection molding industry – for continuous extrusion, because there are no accumulator heads involved in the process, just screws/barrels and dies/mandrels. But if you do operate accumulator-head blow molders – which are a subset of intermittent extrusion blow molding, and best-suited for large-sized high-density PE (HDPE) products – there are a number of considerations necessary for a good purging outcome. Choosing the right CPC, already mentioned above, is particularly important with accumulator-head machines. “Accumulator heads can be incredibly difficult to clean, so always buy the compound from a trusted source, one with knowledge of the type of accumulator-head blow molding machines your company uses,” said Ottmar Brandau, president of blow molding machinery supplier PET All Manufacturing. “This is critical, because if a compound contains the wrong chemicals, these can seriously damage the heads and screws. That would lead to even worse production issues.” To begin, cleaning accumulators on blow molding machines typically requires the use of a CPC volume of two or three times the accumulator capacity, some suppliers say. “The steps involved are to fill to 100 per cent and then push out 25 per cent; fill to 100 per cent and then push out 50 per cent; fill to 100 per cent and then push out 75 per cent; and fill to 100 per cent and then push out the full 100 per cent,” Eric Despotovich said. Purging the accumulator head must be performed on a regular basis to ensure that the industrial accumulators are running as efficiently as possible, some suppliers say. “Not only does purging enable accumulator heads to operate at higher speeds and temperatures, but it also allows for improved product quality and reduced maintenance costs,” Ottmar Brandau said. For injection blow molding, meanwhile, customers can follow standard purging guidelines to a certain extent. “Make sure that nozzles are balanced to at least 90 per cent for optimal processing, and then back the injection unit away from the
manifold and follow standard injection molding purging procedures,” Eric Despotovich said. “Once the screw and barrel are free of contamination, move the injection unit back up to the mold and begin to extrude the CPC into and through the manifold with the injection mold open.” Crucially, he continued, don’t close the mold. “Extrude roughly one-half barrel capacity through the manifold and then, using the remaining one-half capacity, run a series of high-velocity short shots through the manifold to maximize pressure and cleaning. And seal the injection unit with a shutdown-approved grade during extended downtime events,” Despotovich said. And for stretch blow molders, some suppliers say, don’t attempt to mold or blow parisons. “Focus on cleaning the injection unit first, by backing it away from the manifold and following standard injection molding purging procedures,” Despotovich said. “To minimize carbon contamination, keep nozzle drool to a minimum, and clean nozzle drool regularly to keep it from entering the manifold. And, at least when using an Asaclean CPC, it’s generally best if added directly to the feed throat, as opposed to being dried with the resin, since the drying process could activate some foaming agents in chemical purges.” And seal the injection unit with a shutdown-approved CPC during extended downtime events, he added. And a popular option for blow molders today, period, is
» CONSIDER IT HANDLED. We design and manufacture material handling systems for filling, unloading, weighing, conveying, and storing all types of plastic materials.
• Integrated Systems • Weigh Systems • Conveying • Mixing and Blending • Container Unloading • Storage Solutions
Smart Solutions to Keep You Moving!
616.738.9000 | sales@ensigneq.com ensignequipment.com
February 2023 Canadian Plastics CPL_Ensign_Feb23.indd 1
15
2023-01-17 1:21 PM
purging
PET preforms purging from black to clear.
single-dose compounds that allow operators to purge their machinery simply by dropping the packets into the feed throat/hopper of the machine.
PREVENTATIVE MAINTENANCE RULES
As a best practice, a periodic purging routine – at the very least – or a strict preventive maintenance purge program should be established to avoid contamination buildup, which could lead to more difficult purging situations requiring greater time and effort. In this, blow molding is no different from injection molding or extrusion. “Normally, a good weekly purge prevents any buildup in the low-pressure areas on lines running
the same material, and we recommend purging for all material and colour changes,” said Bob Grzegorek. “Corrosive materials such as polyvinyl chloride [PVC] should be purged whenever the machine goes down. Lastly, if a machine is shut down for any extended period, a shutdown ‘sealing’ purge should be performed to minimize degradation due to oxidation.” The goal, of course, is to purge often enough to stay ahead of any problems without overdoing it and wasting material. “The best option is to use a CPC to prevent carbon from building up in the first place, and taking preventative steps is always the best way to go,” Ottmar Brandau said. “Too-frequent use becomes time-consuming while cutting into the company’s profits, however, so use a CPC only at regular intervals.” One way to give yourself a break here is to give the CPC a break. “Run the machine to get as much material out as you can before purging,” said Jeff Lewis, sales and technical manager with Slide Products. “Otherwise you’re just using the CPC to push out material instead of to remove what’s underneath, which is what the compound is meant to do.” From the outside looking in, there’s still too much machine time being wasted by blow molders running homebrews and/ or scrap until the changeover can be complete. Although perhaps not as many as before the COVID-19 crisis drove up resin prices. “Before the pandemic, the high cost of CPCs, especially for blow molding, made processors more willing to settle on homemade solutions, even if they had to use five times as much for a purge,” Lewis said. “But now even regrind has a visible cost, so more blow molders are actually buying CPCs.” Which is good, because CPCs for blow molding have gotten much better. While the nuances of blow molding still make purging challenging at first, a consultation with a purge expert can help your company choose the right CPC and use it correctly. In short, if there’s ever been a time to introduce a smart purging program for blow molders, it’s now. CPL RESOURCE LIST Asahi Kasei Asaclean Americas Inc. (Parsippany, N.J.); www.asaclean.com; 800-787-4348 Chem-Trend L.P. (Howell, Mich.); www.chemtrend.com; 517-545-7980 Dyna-Purge Div./Shuman Plastics Inc. (Depew, N.Y.); www.dynapurge.com; 866-607-8743 Pet All Manufacturing Inc. (Toronto); www.petallmfg.com; 905-305-1797 Slide Products Inc. (Wheeling, Ill.); www.slideproducts.com; 800-323-6433 AceTronic Industrial Controls Inc. (Mississauga, Ont.); www.acetronic.com; 905-564-7227 Techmer PM LLC (Clinton, Tenn.); www.techmerpm.com; 865-457-6700
16 Canadian Plastics February 2023 PCS_TempControl_CP_3-375x5_011723.indd 1 CPL_PCS_Feb23.indd 1
www.canplastics.com 1/17/23 10:32 AM 2023-01-18 9:25 AM
APRIL 2023 ISSUE
Here’s an early look at what’s inside the upcoming April 2023 issue of Canadian Plastics magazine: The cover story will be on lightweighting in injection molding. Lightweight materials often translate into less economic costs and less energy consumption. Here’s a look at some of the latest resins powering the increased demand for lightweight parts. In addition, we’ll also feature articles on • Basic tips for a better conveying process • The latest developments in chillers • High-productivity polymer 3D printers
eNewsletters Sign up for our free enewsletters to stay up-to-date Scan QR code
Subscribe to Canadian Plastics Magazine Reading someone else’s copy of Canadian Plastics magazine? Get your own copy by subscribing here. Scan QR code
Looking to market your company to Canada’s plastics industry, contact: Stephen Kranabetter, Associate Publisher | skranabetter@canplastics.com | 416-510-6791
rotational molding
MANUNOR WANTS TO DO MORE Even as it marks 30 years in business, this Sherbrooke, Que.-based rotational molder is all about looking ahead.
By Mark Stephen, editor
I
f plastics processing can be compared for a moment to The Beatles, then rotational molding is George Harrison: the quiet one. But as with Harrison writing such classics as “Something” and “Here Comes the Sun,” rotational molding, also known as rotomolding, can surprise you sometimes. A case in point is Sherbrooke, Que.-based rotomolder Manunor, which has been making some noise of its own over the past few years by designing and manufacturing a series of innovative products, building a new 10,000-square-foot facility adjacent to its main 90,000-square-foot plant in Sherbrooke’s Gene H. Kruger Industrial Park, and investing in new machinery that includes a massive new rock-androll machine from equipment maker STP Rotomachinery.
DEEP ROOTS
Manunor was founded in 1993 by Jacques St-Pierre, who’s impact in the rotomolding world is considerable – he had previously founded STP Rotomachinery in 1988, which is also headquartered in Gene H. Kruger Industrial Park, and which makes a wide range of rotomolding machines and accessories. Jacques St-Pierre was serving as Manunor’s CEO when Manunor entered a very busy period beginning in 2014, which is when it broke ground on a 10,000-square-foot expansion and also
18 Canadian Plastics February 2023
developed two new innovative products. The first was a parts washer for machine shops and vehicle repair shops that allows oil and grease to be thoroughly cleaned without contaminants. The second was an innovative technology for rotomolding stand-up paddleboards for the Quebec-based manufacturer Pelican, and which began large-scale production in fall 2014. Fast forward to today and the firm’s busy period continues basically uninterrupted save for a brief, unavoidable pause during the early days of the COVID-19 pandemic. Jacques St-Pierre has retired from Manunor – and he sold STP Rotomachinery in 2005 – and his daughter Marie-Michelle St-Pierre now serves as Manunor’s general director and CEO, having joined the firm in 2012. Unlike with some family-owned firms, however, her long-term involvement wasn’t a given. “I basically grew up at Manunor, working here on weekends and during summers while I was in high school, but I wasn’t sure about making it my career,” Marie-Michelle said. “I studied mechanical engineering at Sherbrooke University and worked at co-op programs in a number of different businesses, big and small, in other sectors, because I wanted to see what opportunities were out there. So, when I finally decided to join Manunor after I graduated, I was fully committed.” Marie-Michelle currently runs
Manunor with her partner Mathieu Rouleau, who has been with Manunor as technical director since 2012. The couple became Manunor’s owners in 2017.
A SNAPSHOT IN TIME
Manunor currently employs about 45 workers; has annual sales that exceed $10,000,000; and has a long list of North American customers, primarily in Quebec, Ontario, and the Northeast U.S. “We make more than 300 products in more than 20 sectors of activity, including kayaks, paddleboards, containers, tanks, indoor and outdoor toys and games, and parts for vehicles such as buses and ATVs,” Marie-Michelle said. “We do everything to make a finished part, from molding to assembly to packaging, and we’re very active in product and manufacturing process development. The parts washer program that we developed in 2014, for example, was an in-house proprietary product that introduced an innovative solution to the market.” Most of Manunor’s products are made from polyethylene (PE), which is the most common material used in rotomolding and which the company buys in bulk by the railcar-load and stores onsite. Almost 10 per cent of Manunor’s parts are molded with recycled PE, Marie-Michelle continued, and the company is integrating an ever-wider range of materials with additives for UV stabiwww.canplastics.com
Manunor’s new rock-androll machine on the shop floor. lization and scratch resistance. Manunor currently has seven rotomolding machines, all supplied by STP Rotomachinery. The newest machine, installed in August 2022, is a rock-androll rotomolder with two sides and two completely independent arms, and is a total of 18 feet long with a 100-inch diameter. “It’s our longest rotomolder – and actually the longest currently being used anywhere in Quebec – and it fits between our largest rotomolder, which has a 120-inch diameter, and our smallest, which has an 80-inch diameter,” Marie-Michelle said. “STP has a great reputation and it’s local, as well, so parts and service are easy to obtain.”
THE ROTOMOLDING DIFFERENCE
For the uninitiated, rotomolding differs from other plastics processing methods like injection molding, thermoforming, and extrusion in that it works in layers. The virgin material and powdered colourant are poured into the mold, and the mold is then closed tight, placed in an oven, and rotated at an even speed – in this way, the plastic is laid down in thin layers of even thickness, regardless of whether or not the mold features corners and curves. After the material is baked, the plastic is cooled inside the mold to ensure that it hardens evenly, and then extracted. But not every plastic part is suitable to be rotomolded. “The part chooses the
Photo Credit: Simon Rancourt
rotational molding
process, not the other way around – it depends on the function you want,” Marie-Michelle said. “Injection molding might be able to accommodate complex designs but it can’t create hollow products. And compared to blow molding, which does create hollow products, rotomolding offers denser walls and thicker corners, which some parts demand. So, if rigidity and strength are important, rotomolding might be the better choice.” Other advantages, she continued, include low-cost tooling in either aluminum or steel; consistent wall thickness; double-wall construction; high durability, since the parts are molded as one solid piece; high stability; and a great appearance, since rotomolding can accommodate surface finishes such as textures, logos, symbols, and lettering. And unlike competitive processes such as blow molding and thermoforming, rotomolding produces no pinch-off seams or weld lines, which gives a finished product without the use of secondary processes. “It’s the best method for making large, one-piece hollow parts and double-walled open containers such as tanks, kayaks, and coolers,” MarieMichelle said.
“Rotomolding isn’t as well known in the plastics space as it should be. We love rotomolding, and we want more people to love it too.” Rotomolding also differs from other plastics processing methods as far as business strategy goes. “There aren’t many rotomolding shops in Canada, or North America, so there’s enough room for everybody,” Marie-Michelle said. “Most of us belong to the Association of Rotational Molders, we all know each other, and we typically don’t compete against each other – we compete against manufacturers making products in other materials, such as metal, that are better suited to rotomolding. These are the new accounts that we want.” And even here,
there’s a built-in limitation as to which new accounts to pursue, based on part dimensions and geography. “Rotomolded parts tend to be large and hollow, which makes them expensive to ship because you’re shipping a lot of air,” Marie-Michelle said. “So, it doesn’t make sense for us to chase new business that’s too far away. Rotomolders tend to stick to their own regions.”
BEYOND THE PANDEMIC
Rotomolding machines take up a lot of space, which cushioned the blow at Manunor slightly when the pandemic hit. “We didn’t have to shut any lines down or reconfigure our operations to create social distancing on the floor because our workers were already spread out,” Marie-Michelle said. “Like almost every other manufacturer in Quebec, we had to close for about five weeks at the very beginning of the pandemic, but after that we were able to carry on as usual.” And even during that five-week lockdown, the company remained productive. “We worked with a customer to design a portable outdoor handwashing station that could be used safely during the pandemic,” MarieMichelle said. “We designed the part, built the mold, and began rotomolding the product, all in six weeks. We’ve delivered about 3,000 units since then.” With the second generation of leadership now firmly in place as it marks 30 years in business, Manunor wants to keep growing. “We’re constantly meeting with companies that are making metal parts and working to convert them into plastics,” Marie-Michelle said. “We’re very diverse – anything that can be rotomolded, large or small, we can do it, and we want to build on that and keep expanding our product range.” The company also wants to draw more attention to rotomolding, period. “Rotomolding isn’t as wellknown in the plastics space as it should be,” she said. “We want to help change that, and we bring local students in for tours as often as we can, to show them what our process is all about. We love rotomolding, and we want more peoCPL ple to love it too.” February 2023 Canadian Plastics
19
technology showcase
FOCUS ON HOT RUNNERS Solution for thermally sensitive or corrosive applications
Xp nozzle system designed for stack molds
Enhanced design simplifies, speeds up installation
Device speeds hot runner inspection process
The new UltraMelt solution from Husky Technologies is suited for very small technical or medical parts made from different grades of polycarbonate (PC), which can easily degrade at certain temperatures or residence times – parts that typically allow for minimal to no variation in surface finish, part quality or colour. UltraMelt is also designed for challenging bioresin applications such as polylactic acid (PLA), polyhydroxyalkanoate (PHA), and cellulose acetate. All of UltraMelt’s molten resin contact surfaces are made from non-reactive materials, which extends the component longevity against the corrosive effects of certain resins and provides optimized control over thermal profile. UltraMelt is customized for each application and available with a variety of gating methods, nozzle sizes, manifold pitches, and actuation styles; and can be used in both low- and high-cavity applications. Husky Technologies (Bolton, Ont.); www.husky.co; 905-951-5000
The new Fusion G3 hot runner system from Mold-Masters incorporates several enhancements (over the previous FusionG2 system) designed to optimize mold design and simplify and speed up installation. Shipped completely pre-assembled, pre-wired, plumbed, and tested, the G3 nozzles incorporate field replaceable heater bands and gate seals so that molders can respond and fix issues quickly on-site, and also have new optional protective nozzle sleeves that help prevent damage to the nozzle heater and thermocouple wiring during installation. Additionally, anti-rotation and valve pin disconnect are now standard features; compact actuators are available as either hydraulic or pneumatic; the position of air/hydraulic lines and cooling lines can be rotated to be set perpendicular or oriented different to one another; and the system can be installed and uninstalled at room temperature to reduce installation time. Mold-Masters (Georgetown, Ont.); www.moldmasters.com; 905-877-0185
20 Canadian Plastics April 2021
Oerlikon HRSflow’s new Xp nozzle series for thin-wall injection molding can withstand filling pressures up to 2,200 bar to achieve fast injection and cycle times and high part consistency in a stable process. Designed for stack mold systems, the series is appropriate for use with hot runner systems for manufacturing thin-wall packaging on smaller injection molding machines – the nozzles fit a maximum plate thickness of about 9.4 inches, allowing the company to supply perfectly symmetrical molds with up to eight-plus-eight drops, with a minimum pitch between cavities of about 2.6 inches and between the nozzle and inlet of 4.7 inches. The nozzles can handle high filling pressures of up to 31,908 pounds per square inch. Other benefits include reduced energy consumption, fast injection and cycle times, and plug-and-play installation. Oerlikon HRSflow (Byron Center, Mich.); www.hrsflow.com; 616-228-6900
With PCS Co.’s new CableXChecker for hot runner inspection, molders can test a 24-pin cable in less than one minute with 100 per cent accuracy, eliminating human error. Best practices call for hot runner systems to be inspected at every mold change for problems such as crimps, plug wear or breakage. These problems need to be addressed promptly or they can disrupt production and cause expensive downtime. The CableXChecker device automates the inspection process. Featuring a carry handle and industry-standard controller connections, the CableXChecker is powered by a single nine-volt battery, and comes in two models: the KTX10121 for testing 12 zones; and the KT1285 for testing 5, 8, and 12 zones. PCS Co. (Fraser, Mich.); www.pcs-company.com: 800-521-0546
www.canplastics.com
technology showcase
App includes VPN access to control hot runners The new EasyAccess 2.0 app from Spark Industries provides users with simplified VPN remote access to its Fast Heat hot runner controls. Capable of being used on a PC, phone or tablet, the app allows users to monitor the HMI and perform tasks such as creating and editing recipes. Other benefits include secure lower-bandwidth connections, with data passed between the PC and the HMI being encrypted for security. The decreased bandwidth usage also makes for a more responsive connection, and frees up bandwidth for other network connections. The user can also change screens, push buttons, or take any other action that can be performed by the local plant floor operator on the HMI. Accessing the server requires one-time activation of each HMI connection, but there’s no limit on the number of users, and that access is free. Spark Industries LLC (Elkhart, Ind.); www.fastheatbyspark.com; 574-606-4243
Visit www.canplastics.com for the latest news, stories, products, videos, photo galleries and industry events
advertising index Advertiser Page Canadian Plastics 17 CCC Plastics 13 Chillers Inc. 7 Davis-Standard LLC 11 Dyna-Purge Div./Shuman Plastics Inc. 5 Ensign Equipment 15 IMS IFC Novatec OBC PCS Co. 16 Plastic Process Equipment IBC Rotogran International 21 Swiss Steel 9
Website www.canplastics.com www.ccc-group.com www.chillersinc.com www.davis-standard.com www.dynapurge.com www.ensigneq.com www.imscompany.com www.novatec.com www.pcs-company.com www.ppe.com www.rotogran.com www.swisssteelgroup.com
You produce it ... We’ll Reduce it! ... Since 1982 North American Built and Priced Right for Today’s Economy » GRANULATORS » BELT CONVEYORS » BLOWER/CYCLONE SYSTEMS » FINES SEPARATOR SYSTEMS
Rotogran granulators are internationally recognized for their superior design, efficiency, durability and competitive pricing. We are the size reduction specialists for the processing and recycling industry. Our rugged equipment is precision manufactured to meet individual customer needs. • Complete range from press side to central. • Chamber construction second to none. • Custom applications our specialty.
MANUFACTURER OF SIZE REDUCTION EQUIPMENT for the Plastics and Recycling industry
4 SIMPSON ROAD, BOLTON, ON L7E 1G9 CANADA Tel: 905-738-0101 | Fax: 905-738-5750 sales@rotogran.com | www.rotogran.com
February 2023 Canadian Plastics CPL_Rotogran_June22.indd 1
21
2022-05-13 9:35 AM
technical tips
The fundamentals of press shutdown By Garrett MacKenzie, plastic411.com
I
n the fast-paced world of plastic injection, success relies heavily upon quick and efficient start-ups and the elimination and avoidance of unplanned downtime. This article will outline potential downtime events that have a direct relationship with poorly performed shutdown procedures, and will also provide a time-based approach to help reduce or eliminate scrap and downtime associated with press shutdown.
HOT RUNNER APPROACH
SCREW FAILURES
Any time mold activity goes idle, it’s time for mold inspection and care. Slide slots and ejector/guide pins are to be inspected for damage/galling/lubrication. And in-press mold storage is vital – the mold should be left with mold halves touching but not under pressure. In addition, DO NOT spray the moveable half with mold cleaner, as this leads to a breakdown of ejector lubrication, causing oil to get on the parts at restart. Instead, spray mold cleaner on a rag prior to cleaning the ejector half.
Screw shutdown conditions frequently cause unneeded downtime and poor start-ups – shutting down without running the screw dry can lead to feed throat bridging, for example, which can require hours of servicing to fix. In addition, “screw wrap” conditions – material attached to screw flights that didn’t melt during barrel-soak – can occur if barrel temperatures are lowered with the barrel full of material, leading to an inability to charge the screw properly to build a shot. Leaving the carriage forward for long periods of time can lead to nozzle drool. Presses in a shutdown state often don’t apply proper pressure to the nozzle tip and sprue bushing, which can lead to material blowback on restart. So, when a press is shut down, back the carriage off, remove material from the barrel, and retract the screw one inch to release pressure and help prevent drooling. This also sets the check ring to a neutral state, which prevents gas buildup in the screw. The sprue bushing should be inspected and cleaned in preparation for restart. The nature of materials such as nylon, acetyl, and PVC may require purging the screw with an inert material such as polypropylene (PP), styrene or a purging compound to prevent degradation.
22 Canadian Plastics February 2023
Hot runners left on for extended periods of time can perform poorly due to overbaked and/or degraded materials, leading to runners/parts breaking at start-up, requiring mold cleaning and repair. With clear polycarbonate (PC), long heat exposure can cause contamination that leads to huge scrap events; also, high fibreglass content left in the hot runner can lead to plugged drops.
MOLD SHUTDOWN
WATER SHORTFALLS
Water shutdown is crucial to downtime and damage prevention. Long-term shutdowns can lead to unnoticed leaks. When a mold isn’t moving, water performance changes! This type of leak can lead to rust, resulting in pulling a mold for service and repair.
THREE-STAGE SHUTDOWN PROCEDURE
The following procedures outline proper purging and shutdown of presses according to three basic time frames, plus a weekend shutdown, all based on using materials such as nylon. If a press will be down for 30 minutes or less, the screw is to be run forward to remove the shot from the barrel; with the screw empty, the screw is to be pulled back one inch; and the purge is removed
from the press bed. If the downtime length is unknown, or longer than 30 minutes but less than 4 hours, the carriage is to be retracted to separate the tip from the bushing; the tip is to be inspected for blowback; the throat and barrel are to be purged completely dry with PP or a purge compound; now, with the screw empty, pull the screw back one inch; the hot runner is to be shut off; and remove the purge from the press bed. If downtime will be four hours or a full shift or longer, the carriage is to be retracted to separate the tip from the bushing; the tip is to be inspected for blowback; the throat and barrel are to be purged completely dry with PP or a purge compound; with the screw empty, pull the screw back one inch; shut off the hot runner; spray the mold lightly with rust preventative; close the mold, not under tonnage, with mold faces touching; shut off the water at the main valves; and remove the purge from the press bed. Finally, for a weekend shutdown, the carriage is to be retracted to separate the tip from the bushing; inspect the tip for blowback; the throat and barrel are to be purged completely dry with PP or purge compound; with the screw empty, pull it back one inch; shut off the hot runner; spray the mold with rust preventative; close the mold, not under tonnage, with mold faces touching; shut off the water at the main valves; and bank the dryer at CPL 37°C or 100°F. Garrett MacKenzie is the owner/editor of plastic411.com in Grand Rapids, Mich., and a consultant/trainer in plastic injection molding. He has provided process engineering expertise to many top companies, and serves on the Education Committee of the Plastic Pioneers Association. Contact him at garrett@plastic411.com. www.canplastics.com
CHECK OUR UPGRADED FEATURES SUPPLIED AS
STANDARD
AT NO EXTRA COST TO YOU!
NEW 2 Way Sensing
Forget about wasteful time-based drying! The Genie is coming in early 2023!
Unleash the
Magic The Genie knows the exact moisture of the pellets prior to drying and then programs the Dryer to control dewpoint, blower speeds, temperatures and most importantly residence/ drying time so the resin is dried to the prescribed moisture level in the shortest possible time.
> Make more parts in less time > Use less drying energy > Make parts that are always dry, but not over-dried The patent-applied Genie is available exclusively for Novatec dryers produced 2016 onward. Sold & Serviced in Canada by Maguire Products Canada, Inc. 905-879-1100 l info@maguirecanada.com www.maguirecanada.com Drying > Conveying > Blending
www.novatec.com 800-237-8379 | genie@novatec.com
© Copyright 2023 Novatec, Inc.