www.canplastics.com
APRIL 2021
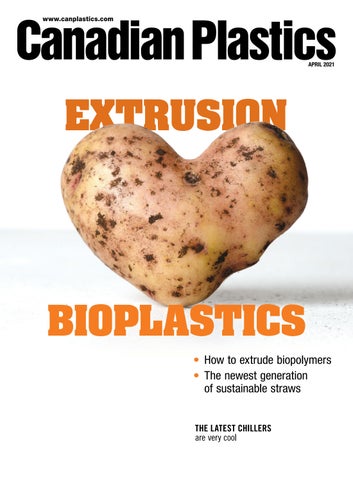
EXTRUSION
BIOPLASTICS • How to extrude biopolymers • The newest generation of sustainable straws THE LATEST CHILLERS are very cool
#MAGUIREMASTERS
Close to 60,000 blenders sold worldwide More standard models than any other producer 30+ years of experience in Gravimetric Blending Industry leading 5 year warranty Are you the next Maguire Master? Call us now to find out more. @MaguireProducts
Maguire-Products
MaguireProducts
info@maguire.com | www.maguire.com
USA Toll Free +1 888 459 2412 | Canada +1 905 879 1100 | Europe +441827 338 280 | Asia +65 6848 7117 | IMEA +971 4 817 0419 | Taiwan +886 4 2658 1535
contents APRIL 2021 VOLUME 80 • NUMBER 2
The March 1960 issue of Canadian Plastics reported on the first major use of HDPE in an automotive application. After 10 months of development work with Phillips Chemical Co., Ford Motor Co. developed front seat side shields made of linear polyethylene for installation on Ford’s 1960 models for North America. “The parts have a lower piece price, lower tooling costs, styling advantages, lighter weight, and increased scruff resistance compared to stamped steel,” our story noted. Toronto-based injection molder Ontario Steel Products Ltd. made the shields for the Canadian cars. Tooling was made by International Tools Ltd. in Windsor, Ont.
Cover Photo: © svetlana_cherruty / Adobe Stock
FROM THE ARCHIVES
10
Number of the month:
$376.8 million*
*Preliminary estimate, in U.S. dollars, of North American shipments of injection molding and extrusion machinery from reporting companies in Q4 2020. (See pg. 6)
18
5 cover stories
4
Editor’s View: Solving the mystery of missing ocean plastic
5
Ideas & Innovations: British Columbia scientists use new bioplastic to make fully compostable coffee pods
10 EXTRUSION: Extrusion loves bioplastics Market demand for biopolymers isn’t just an ecologist’s dream – consumers and retailers want them too. Extrusion shops looking to go along have to be aware that bioplastics come with a unique set of concerns. But if you understand and overcome them, you can reap the benefits of going green.
12 BIOPOLYMERS: Back to Earth 2.0 6
News: • GN Thermoforming bought by Brown Machine Group • Machinery shipments up nearly 20 per cent in Q4 • Plast-Ex trade show moved from May to November • People and Supplier News
20 Technology Showcase 21 Advertising Index 22 Technical Tips: Seven ways to lower injection molding costs
A new generation of made-in-Canada compostable straws is about as sustainable as you can get.
features
14 CHILLERS: Very new and very cool Molding plastic parts requires a huge amount of heat and the transfer of that heat from the plastic and the plastic process equipment, which is where chillers and temperature control units come in. With that in mind, here are some of the latest cooling technologies for your consideration.
18 BLOW MOLDING: The trip from Italy Italian machinery brand Plastiblow is partnering with equipment supplier Globeius to make its all-electric blow molders available again in Canada and the U.S.
Visit us at www.canplastics.com April 2021 Canadian Plastics
3
editor’s view
Canadian Plastics magazine reports on and interprets developments in plastics markets and technologies worldwide for plastics processors, moldmakers and end-users based in Canada.
www.canplastics.com
Solving the mystery of missing ocean plastic
M
icroplastics are in the news for all the wrong reasons lately. In rivers and on seafloors and at the bottom of the ocean, scientists are identifying the highest levels of microplastics ever recorded. A widely reported analysis of sediments pulled from the bottom of the Mediterranean Sea near Italy in May 2020, for example, found up to 1.9 million plastic pieces per square metre, and these findings are believed to be typical. Every day approximately eight million pieces of plastic pollution find their way to the ocean, so we all know it’s a problem – the good news now is that researchers are finally starting to ask the right questions about how to solve it. A new article coauthored by Bruce Sutherland, Professor of Physics at the University of Alberta in Edmonton – and which was posted on The Conversation, a website run by the Academic Journalism Society – looks at the problem of where, specifically, plastic pollution goes when it enters the ocean. The article begins by noting that of the estimated ten million tons of waste plastic that enters the ocean annually, roughly half of that is less dense than water and should therefore float. But according to best estimates, there are only about 0.3 million tons of plastic floating at the ocean surface. So, where’s the rest of it? As Sutherland and his coauthors note, this is the point where microplastics factor in. Ranging in size from five millimetres to specks smaller than bacteria, ocean microplastics are created when larger floating plastic items are broken apart gradually into much smaller pieces by waves and ultraviolet radiation from the sun. Some microplastics are eaten by fish, some develop organisms growing on their surfaces that cause them to sink, and some are washed up onto
4 Canadian Plastics April 2021
Reader Service Print and digital subscription inquiries or changes, please contact Barb Adelt, Audience Development Manager Tel: 416-510-5184 Fax: 416-510-6875 email: badelt@annexbusinessmedia.com Mail: 111 Gordon Baker Rd., Suite 400 Toronto, ON M2H 3R1
beaches and settle into the sand to become land pollution. “With all these complicating factors, it may seem hopeless to predict where microplastics ultimately end up,” the article said. “But we’re slowly making progress.” The progress involves work by a range of scientists around the world to understand how a phenomenon known as the Stokes drift – which, in a nutshell, is the average velocity of something as it travels with the fluid flow – affects floating waste plastic. “For particles smaller than 0.1 millimetres, moving through seawater is like us wading through honey,” Sutherland and his coauthors note. “But the viscosity of seawater has less of an influence on plastics larger than one millimetre. Each wave gives these bigger particles an extra push in its direction.” As Sutherland and his coauthors observe, current research suggests that this might mean larger plastics are carried out to sea much faster than microplastics, making them less likely to settle in parts of the ocean where more marine life is found – around coasts. “A recent study found that non-spherical particles align themselves with the direction of waves, which can slow the rate at which they sink,” the article said. “Lab experiments have further shown how the shape of each plastic particle affects how far it’s transported. Less spherical particles are more likely to go further from coasts.” The idea of applying the Stokes drift in order to understand how waves influence floating waste plastic is new, and unlocking this mystery matters because finding out where all that missing plastic goes can help us figure out which parts of the ocean are most affected by this type of pollution – and where clean-up efforts should be focused.
EDITOR Mark Stephen 416-510-5110 Fax: 416-442-2230 mstephen@canplastics.com ASSOCIATE PUBLISHER Catherine McDonald 289-921-6520 cmcdonald@annexbusinessmedia.com ASSOCIATE PUBLISHER Stephen Kranabetter C: 416-561-5362 W: 416-510-6791 skranabetter@annexbusinessmedia.com MEDIA DESIGNER Svetlana Avrutin savrutin@annexbusinessmedia.com ACCOUNT COORDINATOR Cheryl Fisher 416-510-5194 cfisher@annexbusinessmedia.com VP PRODUCTION / GROUP PUBLISHER Diane Kleer dkleer@annexbusinessmedia.com COO Scott Jamieson sjamieson@annexbusinessmedia.com PRINTED IN CANADA ISSN 008-4778 (Print) ISSN 1923-3671 (Online) Publication Mail Agreement #40065710 2020 SUBSCRIPTION RATES 5 issues Canadian Plastics, plus Dec. 2021 Buyers’ Guide: CANADA: 1 Year $77.50 plus applicable taxes; 2 Years $123.50+ taxes USA: $176.00 (CAD) / year FOREIGN: $201.00 (CAD) / year
Occasionally, Canadian Plastics will mail information on behalf of industry related groups whose products and services we believe June be of interest to you. If you prefer not to receive this information, please contact our circulation department in any of the four ways listed above. Annex Privacy Officer privacy@annexbusinessmedia.com • Tel: 800-668-2374 No part of the editorial content of this publication June be reprinted without the publisher’s written permission ©2020 Annex Business Media. All rights reserved. Opinions expressed in this magazine are not necessarily those of the editor or the publisher. No liability is assumed for errors or omissions. All advertising is subject to the publisher’s approval. Such approval does not imply any endorsement of the products or services advertised. Publisher reserves the right to refuse advertising that does not meet the standards of the publication. MEMBER: Magazines Canada, Canadian Plastics Industry Association.
Mark Stephen, editor
mstephen@canplastics.com www.canplastics.com
ideas & innovations
Photo Credit: University of British Columbia
British Columbia scientists use new bioplastic to make fully compostable coffee pods
Dr. Zac Hudson and a Nexe pod.
C
offee is supposed to help you unwind, not make you feel even more stressed. So, if you’re concerned about your single-use coffee pods ending up as pollution, you can now relax a bit over your morning cup, thanks to a new fully compostable coffee pod design created by a University of British Columbia (UBC) scientist and Surrey, B.C.-based Nexe Innovations Inc. Called the Nexe pod, the pods compost completely in as little as 35 days in industrial compost, and are the result of a three-year collaboration between UBC’s Dr. Zac Hudson, an assistant professor and Canada Research chair in sustainable chemistry, and Nexe Innovations, which is a leader in plant-based materials manufacturing. The problem to be fixed was that many compostable pods already on the market are soft-bottomed, exposing the coffee grounds to moisture and air and allowing them to go stale quickly; and they also hold fewer coffee grounds than plastic pods, which makes for a relatively weak brew. But the downside of pods made from traditional plastic is that they don’t decompose in landfills. So, in order to create a fully compostable pod, the team needed a bioplastic – and, as it turned out, had to formulate a new one. “We started out by importing bioplastics from overseas and trying them out for the pods we wanted to create,” Hudson said. “This helped us learn which materials worked well
and which didn’t, so we could create new formulations inhouse or with the help of our partners.” The team eventually settled on a two-part solution made from two specially engineered components: a bioplastic inner capsule made from polylactic acid (PLA) compounded with other natural ingredients that addresses moisture, air, and heat issues, and holds a large volume of coffee grounds; and an outer jacket made from bamboo that still looks and feels like plant fibre. The new bioplastic was tested in collaboration with Hudson’s research group at UBC, while the composting of the pods was tested at the Surrey Biofuels Facility. “We’re now making our own bioplastics at our facility in Surrey, and are looking to bring significant bioplastics manufacturing capacity to Canada,” Hudson said. “We’re also working on home composting solutions for our pods.” The pods are compatible with all Keurig K-Cup brewing systems, and were launched commercially in January under Nexe Innovation’s Xoma Superfoods brand – and sold out the entire launch inventory through their online store in one day. The company recently announced Nespresso-compatible pods set to begin production later in 2021. Which means that, in future, if your coffee leaves you feeling jittery, don’t worry – it’s the caffeine, not guilt about plastic waste in the environment. CPL April 2021 Canadian Plastics
5
news
GN Thermoforming bought by Brown Machine Group
A GN Thermoforming machine. Photo Credit: GN Thermoforming Equipment
Nova Scotia-based plastics processing machinery maker GN Thermoforming Equipment has been acquired by Brown Machine Group (BMG), a thermoforming machinery, tooling, and automation systems maker headquartered in Beaverton, Mich., which purchased 100 percent of the stock. The financial terms of the deal have not been disclosed. The acquisition significantly expands BMG’s thermoforming product offering and gives the company greater access to global customers in the food packaging industry, a March 1 news release from BMG said. Founded in 1981 and based in Chester, N.S., GN builds thermoforming machines primarily for the food packaging industry, but it also serves the automation, electronics, medical, and plastics markets. “BMG’s proven expertise in growth through acquisition is an exciting and significant step for GN Thermoforming Equipment and our employees,” GN president Jerome Romkey said in the release. “Bringing our core technology, equipment, and service offerings together, while expanding the overall scope of our customer base, is the next logical step for both companies.” GN will continue to operate and manufacture under its current name within BMG and remain headquartered in Chester. CPL
Machinery shipments up nearly 20 per cent in Q4 Marking the third consecutive quarter of growth, shipments of injection molding and extrusion machinery increased 19.3 per cent in North America in the fourth quarter of 2020 compared to 2019, according to the Plastics Industry Association. Based on statistics compiled and reported by the Washington, D.C.-based trade group’s committee on equipment statistics, the preliminary estimate of shipment value from reporting companies totalled US$376.8 million, which was up 22.9 per cent from the third quarter, according to a news release from the association. The industry also saw a 15.8 per cent increase between the previous quarters, the association said. The value of shipments of single-screw extruders led the double-digit growth, climbing 31.6 per cent, while twinscrew extruder shipments were up 4.5 per cent in the last quarter of 2020. Shipments of injection molding equipment rose 23.1 per cent from the previous quarter and were 21.2 per cent higher than the fourth quarter of 2019, the trade group said. Three back-to-back quarters of double-digit increases in plastics machinery shipments underscores the importance of plastics machinery in the manufacturing supply chain, according to Perc Pineda, chief economist for the trade group. “We were hoping to see an increase in shipments of machinery in the fourth quarter as the economy stayed in the recovery cycle and that’s exactly what we got,” he said. “Against the backdrop of a recovering domestic and global economy, the growth momentum in plastics end-markets that began in the second half of 2020 is expected to continue through 2021, which should sustain a steady demand for plastics materials and resin, products, machinery, and molds for plastics.” Canada and Mexico remained the top export markets for U.S. equipment suppliers. The combined quarterly exports to the U.S.-Mexico-Canada trade partners totalled US$173.4 million, which represents 48 per cent of total U.S. plastics CPL machinery exports.
Polystyvert enters PS recycling tech deal with Ineos Styrolution Montreal-based clean technology company Polystyvert Inc. has struck a joint development agreement with German styrenics producer Ineos Styrolution to improve recycling of polystyrene (PS). Polystyvert uses a patented dissolution technology to process PS waste into high-quality recycled PS, officials said in a Feb. 2 news release. The method takes plastic waste in its solid form and dissolves it in a solvent. Once dissolved, the process can mechanically and chemically separate contaminants and additives, before finally separating the original polymer from the solvent. The end product is a cleaned polymer that can be used as new raw material resin again, and the
6 Canadian Plastics April 2021
recycled PS pellets can then be used to make a variety of PS products, including food-grade applications. “The purification capacity of Polystyvert’s technology is unique,” said Ricardo Cuetos, standard products vice president for Ineos Styrolution Americas. He added that the high quality of the final recycled PS resin “is essential to achieving a truly circular economy in key markets like food service packaging.” It’s the second time in three years that Polystyvert, which was founded in 2011, has partnered with a materials firm to advance its technology. In May 2018, the firm announced a deal with the polymer unit of France-based Total SA. CPL www.canplastics.com
Your success is our priority.
Your products impact the world. That’s our motivation for engineering tailored pipe and profile extrusion equipment for your process. When you succeed, your customers succeed. And together, we win.
Call +1 860-650-4270 today to discover the difference!
davis-standard.com
news
Plast-Ex trade show moved from May to November The Advanced Design & Manufacturing (ADM) Expo Toronto trade show – including Plast-Ex, Ontario’s only dedicated plastics show – has been rescheduled from May 2021 to Nov. 9-11, 2021 at the Toronto Congress Centre. In a statement, show organizer Informa Markets said the move to November “allows additional space planning and
safety protocols, plus new features, education formats, and networking opportunities.” In addition to Plast-Ex, ADM Expo Toronto features Automation Technology Expo (ATX), Design & Manufacturing (D&M), PackEx, and Powder & Bulk Solids (PBS) on one show floor. CPL
PEOPLE
Andrew Alaya
Stefan Buchner
Bruce Chinn
Jeff Collier
Arturo Hoyo
Jesus Crespo
Curtis Hatchitt
Charles de Forges
Jimmy Teo
Thomas Gangl
Jonathon Kuhman
Greg Louder
Apala Mukherjee
Jessica Poliner
Kim Povlsen
Nick Sharkey
Paul Swietlinski
Kamal Tiwari
– Extrusion machinery maker Davis-Standard LLC, headquartered in Pawcatuck, Conn., has named Andrew Alaya as vice president, aftermarket sales. – Lossburg, Germany-based injection molding machine maker Arburg has named Stefan Buchner as managing director of its AMKmotion GmbH + Co KG division, which supplies electric drive, control, and industrial automation technology. – The Woodlands, Tex.-based materials maker Chevron Phillips Chemical Co. has named Bruce Chinn as CEO. – Thermoplastics resin distributor Nexeo Plastics, headquartered in The Woodlands, Tex., has named Jeff Collier as chief commercial officer of North America, and Arturo Hoyo as vice president of sales for North America. – Westlake, Ohio-based precision dispensing equipment maker Nordson Corp. has appointed Jesus Crespo as vice president leading its polymer processing systems division, and Curtis Hatchitt as market development manager for pelletizing. – France-based robotic automation maker Sepro Group has named Charles de Forges as CEO; and Jimmy Teo as regional managing director of South East Asia, heading its new sales office in Singapore. – Vienna, Austria-based chemical company Borealis has named Thomas Gangl as CEO.
8 Canadian Plastics April 2021
– Glycon Corp., a Tecumseh, Mich.-based manufacturer of feedscrews and other melt stream solutions, has named Jonathon Kuhman as president and chief operating officer. – Overland Park, Kan.-based UEI Group, which owns hot stamping and embossing equipment makers Universal Engraving and Infinity Foils Inc., has appointed Greg Louder as sales representative for Ontario and Quebec. – Mississauga, Ont.-based chemical maker BASF Canada, a subsidiary of BASF SE, has appointed Apala Mukherjee as president. – Industrial technologies supplier Barnes Group Inc., headquartered in Bristol, Conn., has named Jessica Poliner as president of Barnes Molding Solutions. – Odense, Denmark-based automation maker Universal Robots has appointed Kim Povlsen as president. – Extruder maker US Extruders Inc., headquartered in Westerly, R.I., has named Nick Sharkey as sales manager for Canada and the Northeast U.S. – York, Pa.-based robotic automations maker JLS Automation has appointed Paul Swietlinski as national sales manager for Canada. – Austintown, Ohio-based Xaloy Holdings LLC, a manufacturer of plasticizing components for injection and extrusion machinery, has named Kamal Tiwari as CEO. www.canplastics.com
news
Ontario Teachers’ buys majority stake in blow molder Logoplaste Photo Credit: Logoplaste
The Ontario Teachers’ Pension Plan Board – once the majority owner of Maple Leaf Sports and Entertainment – is now the majority owner of Portugal-based blow molder Logoplaste SA. Ontario Teachers’ acquired the majority stake in Logoplaste from investment firm Carlyle Group, officials said in a Feb. 26 news release. Current Logoplaste shareholders and executives Filipe de Botton and Alexandre Relvas will retain their approximately 40 per cent stake in the firm. The financial terms of the deal were not disclosed. Logoplaste was founded in 1976, and makes plastic bottles and containers for water, milk, ketchup, shampoo, and lubricants, and supplies to Danone, Nestle, Arla, Kraft Heinz, Procter & Gamble, and L’Oreal among others. It operates at 62 locations in 16 countries. CPL
CPL_DecBuyGuide20_Wittmann1.indd 1
Balcan acquires film maker Nelmar Group Canadian film extruder Balcan Plastics Ltd. has purchased Montreal-based Nelmar Group, which includes Nelmar Security Packaging Systems Inc., Plastixx Extrusion Technologies Inc., and Plastixx FFS Technologies Inc. The financial terms of the deal have not been disclosed. Nelmar Group produces extruded film, form-fill-seal films and plastic valve bags, and tamper-evident security packaging. The deal with St. Léonard, Que.-based Balcan will further the long-term growth objectives of Nelmar, a Feb. 16 news release said, and “will enhance Balcan’s existing portfolio of products.” CPL
SUPPLIER NEWS – Soma, a Czech Republic-based producer of flexographic printing presses, plate mounters, and slitter rewinders, has named DTM Flexo Services, of Stoney Creek, Ont., as its sales agent for Canada.
April 2021 Canadian Plastics
9
2019-11-20 11:55 AM
extrusion
EXTRUSION Market demand for bioplolymers isn’t just an ecologist’s dream – consumers and retailers want them too. Extrusion shops looking to go along have to be aware that bioplastics come with a unique set of concerns. But if you understand and overcome them, you can reap the benefits of going green. By Mark Stephen, editor
R
evolutions are never painless – not even the ongoing “green revolution,” in which bio-based plastics are playing a big part. Consumers, and therefore the big-box stores and myriad other retailers that serve them, love bioplastics – which are made from renewable biological sources, not petrochemicals – for their smaller energy and environmental footprints. For many plastics molders, however, it’s more like a love/hate relationship since, from a processing point of view, biopolymers come with a unique set of concerns not found in more common petroleum-based polymers, including moisture, process variation, and sensitivity to temperature and residence time. Which makes this a concern for extrusion shops whose customers are being forced by their customers to use higher amounts of these alternative materials. And there are more of these customers all the time as, around the world, new environmental protection regulations come into force. The end result is an increase in the number of
Davis-Standard’s DS-Blend feedscrew for single-screw extruders is said to work well for biopolymers. Photo Credit: Davis-Standard LLC
10 Canadian Plastics April 2021
extrusion shops that are now processing bioplastics on either a part-time or a fulltime basis. “Extruding bioplastics is definitely a growing trend, especially over the past two or three years,” said Dean Elliott, technical processing manager with Entek Extruders. The good news is, there are steps you can take to make it easier – and even pain-free – to successfully extrude these materials.
ADAPT OR FAIL In the first place, since processors that use bioplastics might have special needs that require customization, it’s important for OEMs to know this in advance before recommending an extrusion solution. “In general, extruding bioplastics is similar to extruding petroleum-based materials, but a few adaptations have to be made,” said Paul Godwin, president and CEO of battenfeld-cincinnati USA. “The most common concern is making sure the screw geometry and tooling design eliminate areas of material degradation due to stagnation. And some bioplastics require a special protection of all surfaces that are in contact with the melt.” According to John Christiano, vice president of technology with DavisStandard LLC, the company’s DS-Blend feedscrew works well with biopolymers. “This patent-pending design improves single-screw performance for demanding applications such as biopolymers by providing distributive and dissipative melt mixing,” he said.
Biopolymers also tend to be temperature-sensitive, which means that extruders dedicated to processing these materials need to have barrel and screw designs that minimize shear. “Most petroleum-based polymers can withstand considerable shear heat, but bioplastics cannot,” Dean Elliott said. An example is extruding film made from polylactic acid (PLA), which has probably the largest production volume of any bioplastic: experts say that while PLA film can be extruded with a generalpurpose screw, output is better with a low-shear screw designed specifically for this resin. And when it comes to co-rotating, twin-screw extruders – which are modular in design and provide for flexibility to adapt – there are some requirements for processing biopolymers that are more difficult to implement after the line has been installed. “Examples would be extending the machine length to add venting capacity and/or moving side feeders or changing feed positions,” said Adam Dreiblatt, director of process technology with CPM Extrusion Group. “Beyond that, modifications to the screw design can accommodate a moderate range of these materials, depending on the specific formulation challenges.”
CLEARING THE HURDLES And one of these challenges is moisture. “With biopolymers, extruders are likely to encounter high and varying levels of moisture,” Dean Elliott said. www.canplastics.com
extrusion
BIOPLASTICS Photo Credit: © svetlana_cherruty / Adobe Stock
“For example, starchbased biopolymers, such as those made with corn or potato starch, may contain up to 12 per cent moisture; and cellulosebased fillers, such as those made from wood flour, have about an eight per cent moisture content.” Polyhydroxyalkanoates (PHA) is another increasingly popular biopolymer, and both it and PLA tend to be hygroscopic, with PLA in particular picking up ambient moisture very rapidly. All of which makes it critical to predry to the recommendations of the resin manufacturer, if required. And usually it is. “Most bioplastics require drying, no different than traditional plastics which require drying before processing to avoid hydrolytic degradation, such as PET,” said Adam Dreiblatt. “The recommended drying conditions – time and temperature – will be provided by the material supplier.” In addition, said Paul Godwin, a vented extruder may be required to remove moisture as well as volatiles. Some bioplastics are designed to be processed at a specific moisture content. And while the bioplastic is invariably supplied at the intended moisture content in moisture-resistant packaging, once the processor receives it, it’s on them to take the necessary precautions to make sure the material doesn’t pick up any unwanted moisture. Keeping packaging tightly sealed when not in use is an obvious step. “Also, we recommend drying the material with a hopper/dryer located directly at the entry of the extruder – this way, there’s no chance of the material coming in contact with moist air,” said Kevin Slusarz, director of process technology with US Extruders Inc. Varying levels of moisture, in com-
bination with the wide variety of possible base polymers and the great differences in formulation, contribute to another challenge of extruding biopolymers: process variation. “With biopolymers, there can be tremendous lot-to-lot variation in melt flow and moisture compared to virgin resin,” Adam Dreiblatt said. “This doesn’t affect the machine hardware itself, but requires different operating conditions such as screw speed, temperature settings, and more, each time to produce the same properties.” Another root source of the problem, according to Kevin Slusarz, lies in the nature of current biopolymer production. “The biopolymer world tends to be more about batches, and whenever you do anything batch to batch, there will be more variation,” he explained. Melt strength is also a characteristic of some biopoloymers that can limit processing rates. “Low melt strength can lead to problems of sagging and nonuniform drawdown during processing,” said John Christiano. “This presents difficulties in forming profile shapes and creating uniform film thickness.”
PROBLEM PREVENTION The flip side to extruding biopolymers is understanding how these materials can impact the extruders. Mainly this means the risk of corrosion inside the barrel caused by all that moisture. “An early preventive step in minimizing corrosion is to specify the correct metallurgy when the extruder is purchased,” Dean Elliott said. “Several special metals can be used inside an extruder for parts that come in contact with materials like PLA.” According to John Christiano, various grades of stainless steel such as 15-5 PH and 17-4 PH work well for corrosion protection when processing PLA
and other biopolymers. “For even higher levels of corrosion resistance, chromium and nickel-chromium alloys may be used,” he said. Later, when a line is down and the material is sitting inside, it’s important to run purges. “Most biopolymer suppliers recommend that the extruder – and molds – be purged completely with an inert resin or purging compound before shutdown to eliminate the possibility of corrosion,” Adam Dreiblatt said. In the end, processing biopolymers is different than processing traditional petroleum-based resins, and experts recommend choosing extrusion components that are optimized for the job. Which means bringing both the material supplier and OEM into the conversation from the outset. “Information from the resin producer is essential to understand the critical processing parameters for a specific biopolymer,” said John Christiano. “After that, it’s always good to check with your OEM regarding available options to deal with these challenges.” It’s the best way to make your participation in the green revolution as painless as possible. CPL RESOURCE LIST Battenfeld-Cincinnati USA (McPherson, Kan.); www.battenfeld-cincinnati.com; 620-241-6843 CPM Extrusion Group (Traverse City, Mich.); www.centuryextrusion.com; 231-947-6400 Davis-Standard LLC (Pawcatuck, Conn.); www.davis-standard.com; 860-599-1010 Auxiplast Inc. (Sainte-Julie, Que.); www.auxiplast.com; 866-922-0282 Entek Extruders/Entek Manufacturing Inc. (Lebanon, Ore.); www.entek.com; 541-259-1068 US Extruders Inc. (Westerly, R.I.); www.us-extruders.com; 401-584-4710 April 2021 Canadian Plastics
11
Photo Credit Left: © naiaekky / Adobe Stock • Photo Credit Right: © sheilaf2002 / Adobe Stock
biopolymers
BACK TO
EARTH
2.0
A new generation of made-in-Canada compostable straws is about as sustainable as you can get. By Mark Stephen, editor
T
he old adage about the best defense being a good offense has probably never felt more real than for traditional plastic straw manufacturers right now, with single-use plastic straw bans becoming ubiquitous – including in Canada, where the federal government plans to eliminate them this year. For Brantford, Ont.-based Stone Straw Ltd. – whose namesake founder patented the artificial drinking straw back in 1888, and which currently is North America’s largest independent dedicated straw manufacturer – the defense began almost two years ago, with the launch of its first version of “Back to Earth” straws made with compostable biopolymers. Fast forward to today and Stone Straw is set to introduce a new, even more compostable generation of the Back to Earth straws made from an
12 Canadian Plastics April 2021
updated cellulose acetate formula based on two very basic building blocks: wood fibre and vinegar. “The biopolymer for our 2.0 version straws is supplied by Eastman Chemical Co., and is derived from wood pulp, or cellulose, grown in responsibly managed forests; and acetate from acetic acid, which is vinegar,” said Abe Looy, regional operations manager at Stone Straw and its parent company Wentworth Technologies. “Cellulose acetate is probably most commonly used in pharmaceutical as a semi-permeable membrane for control release tablets, and it’s extremely degradable.” According to Looy, the first generation of Back to Earth straws was made from a proprietary, functionalized variation of standard PLA, which required modifications on Stone Straw’s extru-
sion machinery – and the 2.0 version straws required modifications on top of those modifications. “Heating plastic to 200°C or 400°F and then cooling it to 25°C or 80°F is the typical, traditional way to extrude profile polypropylene [PP] straws,” he said. “We had to reverse that to extrude this new straw: it comes out in a hot molten state and then enters a water bath heated between 40° to 60°C or 100° to 140°F, which gives it time to relax and bind together, followed by a rapid cooling from a finely controlled absolute air ring. And because it’s a far more sensitive, unforgiving material than traditional PP in a molten state, we had to learn to float the straw in the water bath so that nothing touches it, because anything that does touch it leaves a line. Finally, the cutting has to be very precise.” www.canplastics.com
biopolymers
LIKE POLYPROPYLENE, ONLY BETTER It may behave like a hothouse flower during production but, once it has cooled down, the final product is just as tough and durable as PP straws. “Post-production, our new straws can be printed and wrapped in the typical fashion just like PP straws, and we’ve had enough learning that we can now compete with typical production speeds for PP straws,” Looy said. And for the consumer, it will behave like a typical plastic straw rather than a paper straw, which turns soggy in a liquid. “Chemically, the straw is similar to a piece of wood – which means that it absorbs moisture – and it becomes supple in a drink and will feel like any PP straw,” Looy continued. But it’s actually clearer than a traditional plastic straw. “We made the necessary drawdowns so the straws are glass-clear, with no opaqueness at all,” Looy said.
CPL_Struktol_MarApril21.indd 1
And after use, the straws are industrially compostable in a commercial composting facility and backyard compostable in a traditional home compost. They will also degrade in soil, water, and marine environments, meeting ASTM D6400 and ASTM D-6691 standards. “On top of that, if the new earth-friendly straws end up in an active landfill, they will degrade and contribute to the production of natural gas, which in turn is used for energy in heating our homes,” Looy said. “This achieves our government’s zero plastic waste and circular economy goals.” Having spent almost a year – in the middle of a pandemic – developing the straws, Looy believes that most of Stone Straw’s heavy lifting on the project has now been done. “Unlike PP, this material isn’t easy to work with, and it
took a lot of trial and error – including product trials conducted virtually, with cameras pointing at the extruders – to develop the right material formulation and processing method,” he said. “Everything has to be perfect, but if it was easy everyone would be doing it, and it’s made us better extruders.” Stone Straw has made sample products and sent them to its current customers, project partner Eastman has guaranteed material for future production, and the new straws are scheduled to be launched late this spring in 5.5and 7.0-millimetre diameters. “We went back to basics for our 2.0 version of Back to Earth straws and made a product that acts, essentially, like a very thin piece of wood and then returns to nature,” Looy said. “It’s a made-in-Canada product we’re very proud of.” CPL
April 2021 Canadian Plastics
13
2021-03-04 9:52 AM
chillers
VERYANDNEW VERY COOL
Conair Group’s new ECO air-cooled chillers are available in six models with cooling capacity ranging from 40 to 120 tons. Photo Credit: Conair Group
Molding plastic parts requires a huge amount of heat and the transfer of that heat from the plastic and the plastic process equipment, which is where chillers and temperature control units come in. With that in mind, here are some of the latest cooling technologies for your consideration. By Mark Stephen, editor
T
here’s a lot of moving parts – literally and figuratively – involved in making a plastic product, but it’s safe to say that plastics processing today simply wouldn’t exist without cooling. Which is why chillers and temperature control units (TCUs) are so crucial. A chilling system cools the hot plastic that’s either injected, blown, extruded or stamped, and can also cool down the equipment that’s used to create plastic parts – the hydraulics of the molding machine, and gear box and barrel of the extruder – to save on energy and on the wear and tear of the machine itself; and TCUs provide control of process temperatures, servicing a single process at any one time, and are designed to be moved between process applications as the need requires. Chiller systems range vastly in size and design, and are available as small, localized or portable chiller units for smaller applications or large central chillers designed to provide cooling for
14 Canadian Plastics January/February 2021
entire processes. There’s something a bit misleading in the fact that, contrary to their name, chillers don’t actually create cold – they remove heat – but otherwise the principle is straightforward: a pumping system circulates cool water or a water/glycol solution from the chiller to the process, and this cool fluid removes heat from the process and the warm fluid returns to the chiller. But that doesn’t mean that nothing new happens in the world of chillers and TCUs. For a discipline that deals with fluids, it’s pretty fluid itself. Here’s a look at some of the latest developments.
GREAT OUTDOORS Designed for outdoor installation, Conair Group’s new ECO air-cooled chillers are available in six models with cooling capacity ranging from 40 to 120 tons, and all feature direct-drive hermetically sealed scroll compressors. Dual refrigeration circuits, with multiple compressors, provide built-in redun-
dancy, while the larger units – 80 through 120 tons – also incorporate independent process fluid circuits as well. “The modular design of the ECO chillers means that multiple units can be connected to a single control interface, providing centralized control of up to 12 temperature control circuits,” said Jim Fisher, Conair’s general manager, heat transfer. Wide ambient operating conditions from -29° to 52°C or -20° to 125°F mean the ECO chillers can operate in all but the most extreme environments, Fisher continued. “An operating setpoint range from -6° to 26°C or 20° to 80°F allows them to meet almost any process temperature requirement,” he said. Controls include Modbus RTU or TCP/IP communications as standard, with other communication protocols available optionally. “ECO chillers are also fully compatible with Conair’s SmartServices cloudbased Industry 4.0 monitoring, management, and analysis,” Fisher added.
Shredders and granulators built for the plastics industry.
888.440.7170 | info.us@weima.com | weima.com
chillers
Thermal Care’s new Accuchiller KSE series of outdoor packaged chillers provides process cooling in a wide range of ambient conditions. Photo Credit: Thermal Care Inc.
Thermal Care Inc.’s new Accuchiller KSE series of outdoor packaged chillers provides process cooling in a wide range of ambient conditions. Offered in a compact, all-in-one package design that minimizes installation cost and maximizes usable space, the integral air-cooled units feature energy saving, variable speed fans and a robust PLC. The control system has extensive diagnostic capabilities and numerous communications options, making it IIoTready. Additionally, the units have a modular design, which allows up to 12 refrigeration circuits to be combined into a single system for as much as 720 tons of cooling capacity. The standard process fluid temperature range of -6° to 26°C or 20° to 80°F is ideal for a wide range of industrial applications, company officials said. And unlike competitive chillers, the chillers require no additional optional equipment to operate within ambient temperatures ranging from -28° to 50°C or 20° to 125°F. The chillers also come with completely independent backup fluid and refrigeration circuits.
VIRTUAL DEVELOPMENT Aquatech, a brand of the Piovan Group, used the recent virtual version of the China Plastics Expo to highlight its CH 280VH series of portable air-cooled chillers. Benefits include flexible functioning, with ambient air temperatures up to 40°C or 105°F; reduced energy absorption and lower noise levels via scroll compressors; a stainless steel brazed plate evaporator; an internal water circulation pump; and safe functioning via high- and low-pressure switches, high-
16 Canadian Plastics April 2021
and low-pressure gauges, metal filters on condensers, and flow switch. Outdoor installation versions are also available.
KILLER COMPRESSORS For chillers and chilling systems maker Temperature Corp., recent developments have centred around compressors – which are the heart of the refrigeration system – and using fan speed control on air-cooled chillers. According to company president Roger Lambert, Temperature Corp. now offers customers a choice of two sizes of DC brushless permanent magnet scroll compressors by Copeland that can operate from 1,200 to 7,200 rpm. “These compressors save in energy as they unload,” he said. “Using it in an air-cooled chiller with 10°C or 50°F leaving water temperature and 35°C or 95°F plant air temperature, the capacity range is 1,800 to 6,600 rpm, and five to 18 tons. And matching the compressor with a speedcontrolled fan both saves energy and gives better control of the water temperature.” Temperature Corp. now also offers high-temperature scroll compressors with Freon 513A for heat reclaim or hot water uses that provides up to 32°C or 90°F entering water to the chiller, and hot water from the water-cooled condenser up to 80°C or 175°F. “We also offer low-temperature scrolls for process chillers down to -17°C or 0°F leaving water/glycol temperature, and the chillers can be configured as air- or water-cooled condensers,” Lambert said. “And all of our chillers are available with an optional chiller controller, keypad display, and communications to a plant PLC.”
Mokon’s new Xtreme-Therm line of portable chillers have scroll compressors that provide efficiency, reliability, and quiet operation with a fluid temperature range of -7° to 18°C or 20° to 65°F, company officials said. Available in air- and water-cooled condensing, the XtremeTherm product line also includes circulating water and heat transfer oil systems, and combination chilling and heating systems with temperatures ranging from -29° to 343°C or -20° to 650°F. The equipment features polyester powder coated heavy-gauge steel cabinets, NEMA 4/12 panel with Z purge system suitable for Class I Division 2 locations, UL 98 disconnect switch, TEFC motors, liquid-filled pressure gauges, and more. Frigel has expanded its family of packaged air-cooled chillers for plastics processing. The MRS line features eight compact chillers that are rated from 3.5 to 15.4 tons of cooling capacity; 8.6-ton and 13.7-ton models are available for use with open extrusion tanks. The chillers have single hermetic scroll compressors and boast a wide operating temperature range; the leaving water temperature setpoint range is from -5° to 25°C or 23° to 77°F. A big benefit of the chillers is versatility, company officials said: The units are available in multiple configurations and can be installed indoors or outdoors. MRS chillers have a pump and tank built in so they can be moved easily from machine to machine.
CONSIDERING TEMPERATURE CONTROL Complying with new pump efficiency guidelines put in place in the U.S. last year by the Department of Energy, Advantage Engineering Inc. recently unveiled newly designed high-flow, high-performance water TCUs for standard temperatures up to 120°C or 250°F. The units are available with 5and 7.5-hp pumps for flow rates up to 100 gallons per minute. Additionally, 10, 16, 24, and 34 kW heaters are available. The systems are controlled by Advantage VE, G or T microprocessor controls for precision temperature control. “The new TCUs replace our older design, and are more efficient – using less power per gallon per minute – and www.canplastics.com
chillers
better performing,” said company president Jon Gunderson. “Most TCUs typically offer between 3 hp and below, so our 5-and 7-hp TCUs are well-suited for bigger molds.” And Wittmann Battenfeld recently introduced the Tempro plus D M120 TCU in single- and dual-circuit versions. Company officials said the product launch was based on market research that revealed strong interest in a directly cooled pressurized unit of the same size as the Tempro plus D M100. As standard, the Tempro plus D M120 supplies direct cooling capacity of 80 kW with a Delta T of 75°C or 165°F. In addition to the standard 9-kW heating capacity, models with capacities of 12 or 16 kW are also available. Wittmann officials note that it only uses stainless steel pumps with wear-free magnetic couplings, which cover a range of maximum flow rates from 40 to 90 litres per minute. A frequency controlled pump with
1.1 kW, 50 litres per minute, and 9 bar is also available. And the new Tempro comes with a Wittmann 4.0 interface as standard, enabling integration of the TCU into the work cell’s control system. As heat removal devices, chillers and TCUs will always have outsized roles in plastics processing. Which is what makes these latest developments so cool. CPL RESOURCE LIST Advantage Engineering Inc. (Greenwood, Ind.); www.advantageengineering.com; 317-887-0729 Chillers Inc. (Newmarket, Ont.); www.chillersinc.com; 905-895-9667 Aquatech/Piovan Canada Ltd. (Mississauga, Ont.); www.piovan.com; 905-629-8822 Conair Group (Cranberry Township, Pa.); www.conairgroup.com; 724-584-5500 Dier International Plastics Inc. (Unionville, Ont.); www.dierinternational.com; 416-219-0509
Industries Laferriere (Mascouche, Que.); www.industrieslaferriere.ca; 450-477-8880 Turner Group Inc. (Seattle, Wash.); www.turnergroup.net; 206-769-3707 Frigel North America (East Dundee, Ill.); www.frigel.com; 847-540-0160 Hamilton Plastic Systems Ltd. (Mississauga, Ont.); www. hamiltonplasticsystems.com; 905-890-0055 Mokon (Buffalo, N.Y.); www.mokon.com; 716-876-9951 En-Plas Inc. (Toronto); www.en-plasinc.com; 416-286-3030 Temperature Corp. (Markham, Ont.); www.temperaturecorporation.com; 877-513-8330 Thermal Care Inc. (Niles, Ill.); www.thermalcare.com; 847-966-2260 D Cube (Montreal); www.dcube.ca; 514-831-6623 Tantus Corp. (Pickering, Ont.); www.tantuscorp.com; 647-258-9657 Wittmann Battenfeld Canada Inc. (Richmond Hill, Ont.); www.wittmann-group.com; 905-887-5355
INLINE ANGEL HAIR TRAP
PROBE BOX
MANIFOLD STATION
LORENZ MANUFACTURES PRODUCTS FOR EVERY STAGE OF THE PROCESS
Ask about Lorenz Lighting Ship USA 1-800-263-7782 | CANADA 1-800-263-1942
CPL_Lorenz_MarApril21.indd 1
ONE STOP SHOP STANDARD 2 WEEK DELIVERY April 2021 Canadian Plastics
17
2021-02-24 9:48 AM
blow molding
Pictured here is a Plastiblow doublesided model PB22ED-700 unit for the production of three-layer containers. Photo Credit: Plastiblow/Globeius
The trip from
By Mark Stephen, editor
ITALY
I
n what could be a big development for North American blow molders, Globeius – a new name for wellestablished equipment business Plastics Solutions USA Inc. – is partnering with Italian all-electric blow molding machine maker Plastiblow to make Plastiblow machines available in Canada and the U.S. Miami, Fla.-based Plastics Solutions/Globeius has been in business for about 40 years and, until recently, focused on the plastics industry in
18 Canadian Plastics April 2021
Latin America. According to general manager Graeme Sands, who is based in Ancaster, Ont., the company was rebranded last year as Globeius to signify that it’s expanding in both product range and geography, and will now serve three market areas: plastics, agriculture, and general industrial. “We’ve had a solid presence in Latin America for the past 16 years and now we want to raise our profile in North America by branching out beyond online catalogue sales to include major
Italian machinery brand Plastiblow is partnering with equipment supplier Globeius to make its all-electric blow molders available again in Canada and the U.S. capital equipment, in particular blow molding machinery,” Sands said. “We’ve already been representing Plastiblow in Latin America and Mexico for more than 10 years.” Founded in 1964 and in business as a blow molding machine maker since 1972, Plastiblow is a pioneer in supplying all-electric units. The firm has had some representation in Canada and the U.S. in the past – and there are a few older systems from the 1990s still in operation in a few shops today – but it www.canplastics.com
blow molding
never made any real inroads, and the company hasn’t been active here for years. But now it’s back in this new joint venture that builds on its relationship with Globeius and, according to Sands, the Plastiblow brand – which consists entirely of all-electric, shuttletype extrusion blow machines, both single- and double-sided, for making parts from 10 millimetres to 30 litres – has a number of factors in its favour. First, he said, they’re less expensive than more familiar all-electric competitors. “More importantly, we believe they have the best price/performance ratio on the market – a 90 to 95 per cent efficiency, or overall equipment effectiveness,” he said. The cleanliness of the Plastiblow electric machines – which don’t spill oil or leak onto the shop floor – is also attractive to most molders, Sands added, especially those in food and
medical packaging. “They’re also more efficient than hydraulic machines, especially during start-up, because there’s no need to wait for the hydraulic oil to warm up,” he said. “And they have the lowest energy consumption in the sector under the same production conditions.”
REGIONAL REPRESENTATION As part of this new push into Canada and the U.S., Plastiblow spare parts are stocked by Globeius in Florida and Mexico, and can be shipped easily into Canada; and the company also plans to have a machine available for demonstrations in Miami. “On the sales and service side, we have two full-time service technicians who are located in Mexico but can travel throughout North America, and we also have regional sales representatives in the U.S. and Canada,” Sands said. “Our representative in
01-8938-COL-CanadianPlastics-Success-7x5.qxp_Layout 1 3/5/21 12:46 PM Page 1
Affordable
Ontario is Steve Sawdon at Wesco Services. Steve and I worked together at Mold-Masters Ltd. back in the 1990s, so we have a well-established connection and a good business relationship. And we’re currently looking for sales representation in Quebec.” Globeius has already installed four new Plastiblow machines in Canada, Sands added. Aside from its expanded blow molding activity with Plastiblow, Globeius represents other plastics-related brands, including Bunting Magnetics, Crizaf conveyors and separators, Moditech granulators, Powertech Components, and commercial purging compound maker Slide Products; and it has its own Plastics Solutions brand of injection shutoff nozzles, mold chutes, insulation blankets, skirts and side curtains, drool shields, Gaylord tilters and covers, hopper loaders, bins, and other material handling equipment. CPL
Experience Full Control
Sepro Success Robots
Include 5-Axis Option Sepro has completely redesigned its bestselling Success Line and now includes a 5-axis servo version. All Success robots feature best-in-class technology: • reliable cam-follower bearings • larger part-handling and wider stroke capacity • more compact footprint • simpler maintenance Success robots are THE most versatile and technological solution for injectors. Seven models are available for IMMs from 60 to 900 tons. www.sepro-group.com • seprocanada@sepro-group.com • 514-515-9349 • @SeproGroup l
CPL_Sepro_MarApril21.indd 1
April 2021 Canadian Plastics
19
2021-03-08 9:21 AM
technology showcase
DRYERS
BLOW MOLDING
App links dryers for centralized control
New HDPE a paradigm shift for blow molded applications
In 2020, Dri-Air Industries Inc. introduced its SmartTouch controls to give Industry 4.0 communication capabilities to its dryers – and now, the company’s new SmartView app advances those capabilities, giving users access to all dryers linked to the network in a facility the ability to monitor and control them from a single desktop computer without any need to walk the plant floor. The SmartView app displays up to four dryers on screen at a time, showing dryer status, dewpoint, hopper status, regeneration status, and IP address. From within the app the user can start or stop each dryer, set hopper temperatures, and even create a customized name for each individual dryer. There is no limit to the number of dryers the app can control. Dri-Air Industries Inc./Maguire Products Canada Inc. (East Windsor, Conn.); www.dri-air.com; 860-627-5110 Maguire Products Canada Inc. (Vaughan, Ont.); www.maguire.com; 905-879-1100
ExxonMobil has introduced Paxon SP5504, an HDPE grade designed to offer a step-change in ESCR (Environmental Stress Cracking Resistance) performance for blow molded bottles and containers without compromising stiffness, impact, top load performance, or processability. Paxon SP5504 fills the space between unimodal and bimodal HDPE grades: it can be used as a drop-in solution for unimodal HDPE but with a better balance of properties, or it can be used to replace bimodal HDPE grades in applications that have had to be over-engineered to obtain a desired balance of ESCR and stiffness. Paxon SP5504 is suited for household and industrial chemical bottles and containers for bleach, wipes, agricultural chemicals, and similar products; and an additional benefit is that post-consumer recyclate content can be increased with minimal impact on its properties. ExxonMobil (Houston, Tex.); www.exxonmobilchemical.com/HDPE; 832-625-4000
INJECTION MOLDING Engel expands its e-speed series With the new e-speed 280, Engel has expanded its hybrid e-speed series into the lower clamping force range, with a particular focus on manufacturers of thin-walled containers and buckets and matching lids. With a clamping force of 2,800 kN, the new unit is designed for injection speeds of between 800 and 1,200 millimetres per second; and the ejector performance has been enhanced with hydraulic ejectors as standard, and electric ejectors available as an option. The machine bed and mold mounting platens have been geared closely to the requirements of thin-walled packaging and the use of molds with a high number of cavities, and the machine absorbs the braking energy from the platen movements and releases the stored energy back to the motor as required – for example, to accelerate the mold mounting platens again. Engel Canada Inc. (Waterloo, Ont.); www.engelglobal.com; 519-725-8488
20 Canadian Plastics April 2021
PACKAGING New mid-volume PET preform molding solution
New from Husky Injection Molding Systems Ltd., the NexPET system is a mid-volume PET preform molding solution designed to let users respond quickly to evolving consumer preferences while achieving the highest levels of value, flexibility, reliability, and sustainability. For established producers, NexPET delivers an agile, reliable solution to accommodate niche brands or smaller run SKUs; and for emerging producers, the new solution is a proven, cost-effective solution that enables fast, low-risk entry into markets. Husky’s NexPET system can run up to a 48-cavity mold and offers up to 25 per cent faster mold changeovers to support a multiple preform design environment, the choice of different screw diameters to maximize production output flexibility, and the ability to run recycled PET pellets to support sustainability initiatives. Husky Injection Molding Systems Ltd. (Bolton, Ont.); www.husky.co; 905-951-5000 www.canplastics.com
technology showcase
MATERIALS New family of sustainable TPEs Audia Elastomers has launched the AudiaFlex family of sustainable thermoplastic elastomers, one of the industry’s first TPE portfolios which meet the sustainability needs of brand owners and consumers. Comprised of sustainably sourced, customizable grades, the AudiaFlex materials mirror the properties of most virgin TPEs and deliver comparable capabilities in terms of haptics, colour, adhesion, and durometer, and can compete in high-performance applications with conventional TPEs, TPVs, and TPU chemistries. The AudiaFlex family includes the OP line of thermoplastic elastomers based on marine waste plastics; the AudiaFlex PC line based on post-consumer recyclate; the AudiaFlex PI materials based on post-industrial sources; and AudiaFlex Bio, which consists of bio-based content per ASTM D6866. All four brands come in hardness from 20 Shore A to 95 Shore A. Audia Elastomers (Washington, Pa.); www.audiaelastomers.com; 724-206-2400
J
Visit www.canplastics.com for the latest news, stories, products, videos, photo galleries and industry events
advertising index Advertiser
Page
Website
Canadian Plastics
21
www.canplastics.com
Davis-Standard LLC
7
www.davis-standard.com
Lorenz Conveying Products.
17
www.lorenzproducts.com
Maguire Products
2
www.maguire.com
Plastic Process Equipment Inc.
IBC
www.ppe.com
Sepro Canada
19
www.sepro-group.ca
Struktol Canada
13
www.struktol.com
Vega Instruments Canada
OBC
www.vega.com
Weima America Inc.
15
www.weima.com
Wittmann
9
www.wittmann-group.com
SNEAK PEEK
J
Here’s an early look at what’s inside the upcoming June 2021 issue of Canadian Plastics magazine:
With the return of summer temperatures and higher humidity, processors’ thoughts turn to drying. Our cover story will look at how Industry 4.0 and IIoT are enabling dryers to become more efficient and to produce higher quality output.
In addition, we’ll also feature articles on: J The growing use of post-consumer resins in packaging
applications J The latest product offerings in robots and automation J New plastics application ideas developed by Canadian
universities
Be sure to visit www.canplastics.com for daily news updates and longer feature articles, and follow us on Twitter, @CanPlastics
CPL_SneakPeek_Marc21TD.indd 1
April 2021 Canadian Plastics
21
2021-03-11 9:31 AM
technical tips
Seven ways to lower injection molding costs By Scott Van Hoven, RJG Inc.
I
njection molding is a cost-effective way to produce parts, but there’s often a significant amount of waste involved, from inefficiencies to user errors, machine damage and downtime, high scrap rates, and more. Here are seven ways to lower your injection molding costs and improve your bottom line.
1.
REDUCE RISK AND COST OF QUALITY
The development of injection molding processes capable of handling unforeseen abnormal variation can be very difficult to predict, exposing you to unplanned risk and expenses due to delivery of unacceptable parts. A better way is to use scientific molding principles to develop a repeatable, robust process; and then after the process has been developed using sensors and technology, you can monitor for a wide variety of common defects in injection molding to ensure 100 per cent quality to your customers.
2.
INCREASE EFFICIENCY THROUGH AUTOMATION
With technology and training, you can automate several areas of production to help make the labour force more efficient. Automation can remove inconsistencies, increase efficiencies, improve quality, and increase available floor space. Part picking, part stacking, and palletizing are three types of useful automations. Process control technology can allow for automated part sorting and alarms to let you know when a process is out of tolerance. This further improves efficiency and accuracy by providing data to allow you to determine the root causes faster.
3.
INCREASE AWARENESS OF PROCESS VARIANCE
By knowing immediately when varia-
22 Canadian Plastics April 2021
tion has occurred in a process, you can fix problems sooner, which means less scrap, higher utilization of machine time, and less money thrown in the trash. You can do this through process control software, cavity pressure monitoring, and training. By ensuring that all technical staff are trained to the same standard, you can be proactive in reducing or eliminating rejects rather than reactive and fighting high scrap levels due to low skill levels and poorly set processes with small or non-existent process windows.
4.
PURCHASE WIDESPECIFICATION RESIN
Resin that has more variation in properties is cheaper, but it can be difficult to validate or maintain dimensions with tight tolerance parts. A classic example is running good production for days and then all of a sudden seeing flash on parts. Usually, this is caused by viscosity, which can often swing 30 per cent in either direction. Using widespec resin can help prevent this, along with using cavity pressure sensors to control the process and minimize the impact of viscosity shifts in material.
5.
LOWER CYCLE TIME
Evaluating the part thickness at the beginning of the project is the first step to determining cycle time. It’s important to question the thickness of the part and how it impacts the cycle time and part performance. Often, we find that the parts have been designed this way because “That’s the way we have always done it,” which can be very costly. Science and simulation help predict design success, so we no longer need to build and test to get results. Ensuring proper part design is one way to lower your overall cycle time. Others include using properly
sized mold temperature control units, or thermolators; and having enough water flow, because if the ability to cool the part to the correct temperature is compromised, the part has to remain in the mold longer.
6.
BUILD MORE EFFICIENT MOLDS
7.
REDUCE MOLD TRANSFER COSTS
To build an effective mold, it’s vital to ensure the water lines are placed in the correct location. You also need to select a metal that transfers heat well but can also withstand the material (specifically material with glass or carbon fibre filler); use turbulent water flow to ensure that the mold can reach thermal stability quickly and maintain that stability throughout a long production run; and, wherever possible, go to a higher cavitation to make more parts in the same amount of time.
Process development applications ensure you can quickly and easily transfer a mold from one machine to another. Machine-specific setup sheets are automatically generated when the mold is transferred, so you can make good parts from the first shot. Those curves can be used in any machine as long as the machine is capable of providing adequate flow rate, pressures, temperatures, and volumes. Save time, energy, and resources by not having to create your own unregulated conversion tools or recreate the process from scratch for each new machine. CPL Scott Van Hoven is the Americas sales and business development manager at RJG Inc., a Traverse City, Mich.-based training and consulting company that specializes in the injection molding industry. Visit www.rjginc.com for more. www.canplastics.com
PPE
ROBOT END OF ARM TOOLING SPRUE PICKING ROBOTS
QUICK CHANGERS & BASE PLATES
9 MODELS IN STOCK SIZED FOR MACHINES FROM 15 TO 300 TONS
ALUMINUM PROFILES & JOINING PLATES
CLAMPS, PLATES & SUSPENSION ARMS
FOR FRAME BUILDING
STEM ASSEMBLIES
GRIPPERS & NIPPERS
VACUUM CUPS - ALL SIZES & MATERIALS
PUSH-IN AIR FITTINGS & TUBING INCH & METRIC SIZES
Quality Products, Fair Prices & Best Service since 1974 www.ppe.com PLASTIC PROCESS EQUIPMENT, INC. e-mail: sales@ppe.com PPE
E A S T
8303 CORPORATE PARK DRIVE MACEDONIA, OHIO 44056 216 -367 -7000 • FAX: 216 -367 -7022 TOLL FREE: 800 -321 - 0562
W E S T
6385 MONTESSOURI STREET LAS VEGAS, NEVADA 89113 702 - 433 - 6385 • FAX: 702 - 433 - 6388 TOLL FREE: 800 -258 -8877
Toll Free: USA, Canada & Mexico
800-362-0706 Order Fax: 800-223-8305
We bring colour into view! Compact pressure sensors and switches with 360° custom-colour status display
256 colours Individually selectable: Measurement in progress Sensor switching Process malfunction
15 cm
Compact design
Hygienic adapter system
Adjustment via smartphone
$525 VEGABAR 39 G½"
www.vega.com/vegabar