BULK MATERIALS HANDLING • POWDER HANDLING • QUARRYING • RECYCLING & WASTE BULK MATERIALS HANDLING • FEEDERS & CONVEYING • PACKAGING • PORTS & TERMINALS MANAGEMENT
FEBRUARY OCTOBER 2017 2026
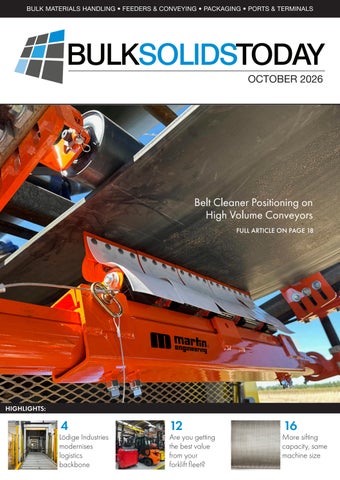
Belt Cleaner Positioning on High Volume Conveyors FULL ARTICLE ON PAGE 18
HIGHLIGHTS:
4
Lödige Industries modernises logistics backbone
12
Are you getting the best value from your forklift fleet?
16
More sifting capacity, same machine size
SOLUTIONS that Power Success TM
BULKBUSTER BULK BAG UNLOADER
CONVEYING LINE
SWITCH RECEIVER
STORAGE SILO
BULK BAG
MODU-KLEEN® BIN VENT FILTER
STORAGE SILO
VIBRA-JET ® BIN DISCHARGE SYSTEM WEIGH HOPPER
BLENDCON® SILO BLENDER STORAGE SILO
DYNA-SLIDE TM HIGH PRECISION AIR-ACTIVATED FEEDER
BAGBUSTER ® BAG BREAKER
BELLA® FLUIDIZED ZONE MIXER AUTOMATIC 15 DEGREE SWITCH
Who We Are
We are a leading provider of custom solutions for the handling of bulk materials for processing businesses across various industries. Dynamic Air has over five decades of expertise in designing and manufacturing pneumatic conveying systems and equipment for handling dry bulk solids.
HDP 4000 FULL LINE CONCEPT ® DENSE PHASE CONVEYING SYSTEM
Our Approach
We never take a cookie-cutter approach just to cut costs up front; we know that the right solution will save you money in the many years to come. Our tailored solutions involve thoughtful planning, meticulous engineering and precise manufacturing that optimize efficiency and productivity.
Dynamic Difference
At Dynamic Air, we set the standard for excellence in bulk solids handling. With a relentless focus on quality, reliability, and customer satisfaction, we deliver reliable, high-quality pneumatic conveying systems, equipment, and custom solutions that exceed expectations.
www.dynamicair.com
Issue 181
BST TEAM Sales Director: Production: Accounts Manager: Office Manager:
James Scrivens Sarah Daviner Avery Hudson Katie Brehm
BULK SOLIDS TODAY is published 6 times a year by Abbey Publishing Ltd
CONTENTS 4
NEWS
12
BULK MATERIALS HANDLING
18
FEEDERS & CONVEYING
To receive a copy free of charge, please send your details to subs@bulksolidstoday.co.uk
21
PORTS & TERMINALS
No part of this publication may be reproduced by any means without prior permission from the publishers. The publishers do not accept any responsibility for, or necessarily agree with, any views expressed in articles, letters or supplied advertisements.
22
PACKAGING
ADVERTISING & EDITORIAL
Please contact us at: Email: editorial@bulksolidstoday.co.uk advertising@bulksolidstoday.co.uk Web: www.bulksolidstoday.co.uk LinkedIn: www.linkedin.com/company/ bulk-solids-today-magazine/ X: www.x.com/BulkSolidsToday
CIRCULATION
30 BUYERS GUIDE
ISSN: 1365/7119 All contents © Abbey Publishing Ltd 2026
www.bulksolidstoday.co.uk Bulk Solids Today
3
COMPANY NEWS
LÖDIGE INDUSTRIES MODERNISES SWIRE COCACOLA HK’S LOGISTICS BACKBONE TO BOOST THROUGHPUT AND OPERATIONAL EFFICIENCY
L
ödige Industries, a leading provider of logistics systems, has successfully completed the comprehensive upgrade and refurbishment of the vertical pallet transport system at Swire Coca-Cola HK’s manufacturing facility in Shatin, Hong Kong. Completed in March 2026, the modernisation project increases throughput by enabling higher traveling speeds for hoists and conveyors, supporting the operational demands of one of Swire Coca-Cola’s largest and most critical beverage distribution hubs in Hong Kong. To mark the completion of the project, Swire CocaCola HK hosted an official ceremony on May 28, 2026. Nicholas Tripptree, Managing Director of AsiaPacific for Lödige Industries, joined the ribbon-cutting ceremony to offer his congratulations. Tripptree praised the close, collaborative partnership between the two companies and highlighted the newly modernised system’s role as a highly resilient backbone for Swire Coca-Cola HK’s daily logistics operations. As the fifth-largest bottling partner of The CocaCola Company globally, Swire Coca-Cola HK holds the exclusive franchise rights to manufacture, market, and distribute Coca-Cola products across multiple key territories, including Greater China. The manufacturing facility in Shatin has been in operation since 1991. To support newly renovated, high-throughput production lines, the facility’s material transportation infrastructure, which previously relied on 11 legacy hoists and conveyor system over 20 years old, required a comprehensive modernization to eliminate operational bottlenecks. Lödige Industries delivered a customer solution that completely fits Swire Coca-Cola HK’s specific operation processes and requirements. Due to the physical limitations of the existing hoist shaft and housing, the company tailor-made and fully replaced the entire setup of 11 hoists according to the precise site conditions. The overhaul also included the removal of an old hoist, installation of new conveyors, interface stations, and an advanced control system. This revamped Bin Hoist System (BHS) has evolved far beyond a simple vertical transport upgrade and now serves as a smart logistics backbone supporting the facility’s daily operations. By introducing a bidirectional function and extending service coverage from floors 3–13 to G–16, the system enables the seamless automated movement of up to 100 pallets per hour, enhancing overall reliability and throughput while supporting future operational demands. Furthermore, the automated solution enhances workplace safety by creating a more controlled environment that reduces internal traffic and reliance on forklifts. This is supported by enhanced enclosures, advanced sensors, and integrated fire protection. Designed with sustainability in mind, the system 4
Bulk Solids Today
incorporates energy-saving features and smart standby modes to minimise unnecessary power usage, helping align the high-throughput facility with modern green supply chain standards. The infrastructure has also been designed for flexibility, offering compatibility with advanced automation technologies to support future operational expansion and digital transformation. The solution was developed using Lödige Industries’ expertise in mechanical and electrical engineering, controls software, system design, installation and commissioning. The upgraded system was tailored to the site’s operational requirements while providing capacity to support future business needs. “Integrating a vertical transportation system into such a high-throughput facility demonstrates how advanced material handling can be applied in demanding, spaceconstrained environments. Beyond boosting efficiency, these systems optimise modern supply chains aiming to reduce energy consumption, minimise forklift traffic, and improve worker safety,” says Tripptree. “We are grateful for Swire Coca-Cola HK’s partnership. Following the successful project handover, Lödige Industries remains by the side of Swire Coca-Cola HK as a reliable partner, securing long-term operational excellence through an established service contract.” www.lodige.co.uk
POWDER METERING MADE SIMPLE
Reliable screw feeding for powders, granules & pellets every time
The NEW Trantec True-Flow screw feeder range offers simpler, proven, and cost-effective solutions for accurate material handling. No unnecessary bells and whistles, just reliable, proven technology designed to deliver consistent performance you can trust.
ACCURATE & CONSISTENT FEEDING Precise material flow for reliable, uniform dosing.
VERSATILE MATERIAL HANDLING
Handles powders, pellets, granules, and challenging materials with minimal blockages and bridging.
Take advantage of our
FREE COST-EFFECTIVE SOLUTION Reliable performance with low maintenance and reduced downtime.
OPTION AVAILABLE
HYGIENIC VERSIONS
Celebrating 30 years of engineering excellence
www.trantec.net
MATERIAL TESTING
To optimise your process
01282 777 566
Scan me
sales@trantec.net
Tool-less dismantling,
EC / FDA
crevice-free design
Food compliant
COMPANY NEWS
JCB INVESTS FOR THE FUTURE AFTER HYDROMAX WORLD RECORD
F
resh from setting a new world land speed record of 406.320mph powered by its pioneering hydrogen technology, JCB is accelerating investment in its future, with major commitments to British manufacturing and new production capacity in the United States. The manufacturer is investing heavily in the transformation of its Staffordshire World HQ, while in the USA, JCB’s new factory in San Antonio, Texas – its largest in the world – opens next month, creating 1,500 jobs over the next five years. As JCB invests for its next chapter, George Bamford is to become Joint Chairman of the family company alongside his father, Lord Bamford. It is the first change at the top of JCB in more than 50 years, during which the business has grown from its Staffordshire roots into one of Britain’s largest privately owned manufacturers, with 23 factories and more than 20,000 employees worldwide. The announcement coincides with JCB reporting a resilient performance in 2025, despite mixed market conditions and geopolitical headwinds around the world. Sales turnover totalled £5.7 billion, profit before tax was £642 million and machine sales reached 113,498 units, while the business remained debt-free with no net borrowings. JCB also increased its global market share, despite flat demand in North America and a 12% market contraction in India. At the heart of JCB’s investment in Britain is the £100 million transformation of its Staffordshire headquarters – JCB’s home since 1950, when Joseph Cyril Bamford moved production into a former cheese factory in Rocester. A £60 million fully automated powder paint plant and a comprehensively modernised shop floor are part of the transformation, helping to secure the future of more than 8,000 UK jobs. In the USA, JCB’s new $1 billion factory in San Antonio, Texas – at 6
Bulk Solids Today
one million square feet, JCB’s largest factory in the world – opens next month. It will build Loadall telescopic handlers and access equipment for North America, the world’s biggest construction equipment market. Investment in factories is being matched by investment in innovation. Hydrogen-powered machines are now in production following JCB’s £100 million programme to develop hydrogen combustion technology, making it the first construction equipment company in the world to bring a fully approved hydrogenfuelled combustion engine to market. Last month, those engines powered JCB into the record books at the Bonneville Salt Flats in Utah. The JCB Hydromax, driven by Wing Commander Andy Green OBE, recorded 406.320mph (653.909km/h) on the Salt Flats to become the fastest ever hydrogenpowered vehicle – more than doubling the previous hydrogen combustion record and beating JCB’s own Dieselmax diesel record, set 20 years earlier. JCB Hydromax was powered by two production-based hydrogen engines manufactured at JCB’s factory in Foston, Derbyshire, and went from idea to world record in just 18 months. Meanwhile, the JCB Academy, a pioneering project championed by Anthony Bamford to address the UK’s engineering skills shortage, goes from strength to strength. This year 708 students applied for 314 places available this September, maintaining the Academy’s longstanding reputation for being heavily oversubscribed. Since opening in
2010, it has educated around 3,750 young people and boasts a 100% record of leavers progressing into employment or further education. This month a total of 116 new apprentices, undergraduates and graduates, selected from more than 6,300 applicants, also joined JCB. JCB Chairman Lord Bamford said: “Last year JCB celebrated its 80th birthday and, as we look ahead, we are investing heavily in the future of the business – from the transformation of our Staffordshire headquarters and pioneering hydrogen technology, to our new factory in Texas. As part of that next chapter, I’m delighted that my son George will become Joint Chairman of JCB. We have never been a company that stands still, and these investments will ensure JCB is well placed to seize the opportunities ahead.” George Bamford said: “From the day my grandfather founded JCB in 1945, innovation and investment in Great Britain has been at the heart of everything we do. JCB Hydromax showed the world what British engineering can achieve. That same spirit is in every machine we build. While JCB has expanded globally over the years, our home has always been here, and the record investment we are making in our facilities and in new products is good news for Britain and good news for JCB.”
www.jcb.com/en-GB/
Challenges with noise and dust? For us it’s no problem.
From large stones to the smallest grains: Bulk solids come in all types, shapes and sizes, but choosing the right measurement technology is surprisingly easy. With our level and pressure sensors, you can effortlessly keep an eye on all your important process values – and still have time to crack the really hard rocks. Everything is possible. With VEGA.
vega.com
COMPANY NEWS
NPC HELPS CR REYNOLDS DELIVER £10.3 MILLION URBAN RENEWAL SCHEME The Holmfirth Town Centre Access Plan is a £10.3 million investment scheme which aims to create a more accessible town centre for businesses, residents and visitors. The scheme aims to help reduce traffic congestion and carbon emissions by prioritising sustainable transport while ensuring accessibility for all and supporting the growth and development of the cultural sector. The working partnership between contractor CR Reynolds and National Pile Croppers (NPC) has enabled the demanding piling work to be completed in a timely and cost effective manner.
T
he Holmfirth Town Centre Action Plan is a partnership project between the council and the West Yorkshire Combined Authority which aims to meet the changing needs of the community. At the core of the scheme is improved traffic flow that aims to reduce journey times which will reduce congestion. In addition, the scheme will provide improved pedestrian safety and delivery enhanced accessibility for vulnerable users. The scheme will involve the demolition of the former market hall building and extension of the adjacent Huddersfield Road car park. LEADING CONTRACTOR IN THE NORTH OF ENGLAND The lead contractor for the scheme is Hull headquartered company CR Reynolds. Founded by Chris Reynolds, the company chairman, it is a privately owned and run organisation that has worked in the UK Civil Engineering and Construction industry for over 40 years. Over this time, CR Reynolds has grown into a well-respected principal contractor with experience in delivering a wide range of civil engineering and building projects across the UK. CR Reynolds possesses a track record of delivering highly quality projects, and this, coupled with a drive for continual improvement, has been reflected in the many industry awards won by the company. CR Reynolds has aimed to always work flexibly and innovatively with its clients and stakeholders, making sure to fully understand each project’s aims and objectives, then deliver them with consistency. This approach has been a major advantage in implementing the Holmfirth Town Centre Action Plan. The company prides itself on its ability to continually meet client’s needs, maintain positive relationships, and deliver a high quality of workmanship, whilst never compromising health and 8
Bulk Solids Today
safety. These simple attitudes being a key characteristic of its business ethics and are best demonstrated by a continuously high level of client satisfaction and repeat business for high profile clients and authorities. MAJOR PILING PROJECT Given the multifaceted nature of the Holmfirth Town Centre Action Plan, a wide variety of concrete piles were required. These were mainly 600mm and 750mm contiguous piles. “The piles are set in a contiguous wall with 10 x 40mm reinforced bars in each cage. The crop section is 1.5m, with 10/11m drilling with no refusal point so the drilling had to go deeper. Hence, and given the nature of the project, and following discussions with CR Reynolds, it was decided to use a CFA with dog-bones and cylinders removed. For flexibility, the cropper was set up to be changed around by the client as quickly and easily as possible to adapt to each pile,” explains National Pile Cropper sales director Scott Fitchett. The NPC CFA hydraulic pile cropper is a traditional linked modular cropper which can be adjusted to
COMPANY NEWS suit required pile sizes. Its flexibility provided to be the ideal solution for dealing with the 600mm and 750mm contiguous piles which were used for the new café and bridge developments. The croppers were used in conjunction with the NPC provided lifting frame. This has the advantage of working with minimal restriction enabling the CFA Cropper to cut circular augured concrete piles from 300mm – 1200mm diameter. It’s modular design further allows for it to be adjusted to suit different pile sizes onsite. Adjustments of 100mm at a time can be achieved easily by adding a half link without any hydraulic interference. TEAM WORK TO THE FORE The nature of the Holmfirth Town Centre Action Plan meant that flexibility of approach was key. “CR Reynold’s attitude throughout enabled us to provide the right and most effective solution,” explains Scott. “They worked with us to find the right solution, telling us of the configuration and then we made it happen. By doing this and by being fully onboard, we were able crop 10-15 600mm and 750mm contiguous piles each day. This doesn’t sound a great deal but due to the nature of the project and the piles, we worked with the CR Reynold’s team try out various setups to get the piles cropped in a tight space. “The NPC team worked tirelessly with CR Reynolds to deliver different setups to achieve a solution. The piles were large, misshapen and very close to one another
requiring a large cropper to fit in very tight gaps which varied from pile to pile. Two different excavators needed to be used for different sides of the river, and the cylinders needed to be moved and removed on the cropper to fit between different piles. CR Reynolds was happy to do this on site when required, drawing on the pile cropping expertise of the NPC team. We visited the site on a continual basis to check progress, monitor the cropper and try to pre-empt any possible issues,” concludes Scott Fitchett of the highly successful working relationship between CR Reynolds and National Pile Croppers. www.nationalpilecroppers.com
Follow BST on social media Tuf-Lok ring grip pipe and tube couplings are rugged, heavy duty, self-aligning and self-grounded couplings with a high end pull. They can be used for almost any application where pipe or tube ends need to be connected. The Tuf-Lok self-aligning couplings install quickly and easily with little effort. Features • Self-aligning • Self-grounding • High pressure rated • Full vacuum rated • Stainless or mild steel • Usable on thin or thick wall pipe or tube • Low cost • Reusable • Absorbs vibration • Externally leakproof
Tuf-Lok (UK) Tel: +44 (0) 1706 822512 Email: sales@tuflok.co.uk • www.tuflok.com
Bulk Solids Today
9
COMPANY NEWS
KEITH MANUFACTURING CO. SHOWCASE RX2 FOR FAST WOOD-PRODUCTS UNLOADING AT RESIDUES-2-REVENUES 2026
K
EITH Manufacturing Co., a global leader in innovative material handling solutions, showcased its RX2 Drive Unit for the Australia and New Zealand wood-products market at Residues-2-Revenues 2026. RX2 is a two-cylinder WALKING FLOOR® drive engineered to rapidly unload chips, sawdust, biomass and similar materials. Visitors are invited to visit Booth 5 to learn how RX2 can help improve turnaround times, support efficient unloading and simplify routine service. The RX2 uses a re-engineered hydraulic sequence to unload a 14.6 meter trailer in about four minutes. In mill operations where truck turnaround affects production flow, this faster discharge capability can support more loads per day and help reduce congestion at receiving areas. Designed with a two-cylinder configuration, the RX2 reduces drive weight while delivering the performance and durability required for wood-products applications. For wood-products fleets operating close to legal limits, the lighter system can create additional payload potential over thousands of loads. RX2 also features an 80% moving and 20% stationary slat configuration, designed to maximize push force while minimizing drag. The layout reduces hydraulic strain, improves energy efficiency and contributes to longer floor life. Part of KEITH’s RX Technology platform, its first major redesign in more than a decade, RX2 is built to address recurring performance and maintenance challenges, including corrosion, difficult component replacement, hydraulic heat and contaminated oil. Its adjustmentfree design removes threaded rods and adjustable switching valves, helping promote consistent operation and reduce long-term maintenance demands. For easier serviceability, RX Technology uses cartridgestyle check valves that can be accessed and replaced quickly with a single wrench. This design helps simplify routine maintenance and minimize downtime. The platform also incorporates integrated heat sensors and automatic over-temperature switches. When oil temperature rises beyond a safe level, the system intervenes by shutting down until temperatures return to a safe operating range, helping protect critical components from heat-related wear, seal damage and efficiency loss. 10
Bulk Solids Today
A high-flow filtration system helps keep hydraulic oil cleaner and reduce contamination in dusty lumber-mill environments. With fewer parts and potential leak points, the simplified hydraulic pathway can further reduce maintenance requirements and the time spent diagnosing issues. RX2 supports intuitive operation through an electric control interface.. Single-action commands simplify training and help reduce operator error, giving drivers more predictable control during unloading. For chips, fines and sawdust, KEITH recommends pairing RX2 with its CleenSweep® tarp system. The CleenSweep system automatically draws a tarp across the trailer floor during unloading, helping reduce leftover material, improve safety and reduce the time operators spend inside trailers. For more information, please visit www.KEITHwalkingfloor.com.
COMPANY NEWS
ROBUST CABLE TRANSDUCERS SIMPLIFY LINEAR TRAVEL MEASUREMENTS
W
hen your OEM or retrofit application requires precise linear measurements, even in harsh, outdoor environments the GCA series of cable transducers, available from sensor specialist Baumer are designed for safe, low-maintenance operation. The key features and benefits of these cable transducers include easy installation, ultra-compact and robust design, combined with long-life components. Together, these key features help to ensure precise measurements, even in the most demanding applications. A key reason for their high precision measurement and long-standing durability, is their precisely guided mechanical winding of the steel cable. Where angled of flexible cable travel is required, optional pulleys are available. Additionally, the cable is sheathed with polyamide, providing protection against corrosion along with superior bending proof performance. Application versatility is assured because they are designed to incorporate a wide range of standard interfaces, enabling quick and simple integration in any control environment, without the need for any additional adjustment aids. In addition, the encoder and cable mechanics are designed to ensure perfect interaction, while high linearity of up to ± 0.01% of the measuring range is available with the flexible GCI/GCA series. When the requirement for cable transducers is for outdoor applications, the compact GCA5series provides robust and space-efficient solutions. With compact plastic housings and protection ratings up to IP67, these options are particularly suited to applications where space is limited, including mobile machines and utility vehicles. The compact GCA series features a three separate chamber principle, providing optimum protection of the electronics and spring mechanism against moisture or other harmful ambient impacts. High-quality components, such as corrosion-proof stainless-steel cable with nylon-polyamide coating and a flat, light shock-proof housing further enhance their suitability for demanding applications. Finally, this broad product portfolio includes compact and flexible cable transducers with a wide choice of interfaces and sensing technologies. The compact GCA series combines integrated sensing with options including analog, CANopen® and SAE J1939 interfaces, while the flexible GCI/GCA series allows the cable transducer mechanics to be combined with a choice of incremental or absolute encoders to suit the application with varying interface options available. Versions with redundant sensing and signal output are also available. For medical technology, logistics and other similar industries the demands are even greater on cable transducers in terms of linearity. This is where the GCI and GCA flexible serieswith metal housings and high position encoder technology meet the most demanding measuring accuracy and service life requirements. They provide at
linearity ± 0.01% of the measuring range up to 50 metres and are ideal for indoor applications. Extremely high accuracy is assured thanks to precise mechanics, guided winding of the cable, combined with precise encoder optical sensing. Their versatility is possible due to cablepull mechanics combined with a choice of incremental or absolute encoders to suit any measuring task. More at: Cable transducers | Baumer Great Britain.
Other Valves Fight Friction, We Designed it Out Unlike other valves that seal with friction, Posi-flate’s unique butterfly valve uses an inflatable seat to seal with air pressure. Thus it requires less torque and a smaller actuator, resulting in lower cost. Plus, the seat automatically compensates for wear, providing longer life. Some users have reported over six million cycles and the valves are still going strong. • • • • • •
Less friction Low torque Low maintenance Lower actuator costs Longer valve life More reliable Tel: +44 (0) 1908 622366
www.posiflate.com
Bulk Solids Today
11
BULK MATERIALS HANDLING
ARE YOU GETTING THE BEST VALUE FROM YOUR FORKLIFT FLEET? Chris Rodger, National Sales Manager at Rushlift, explains how taking a holistic approach to forklift fleet management can drive performance and value.
M
any businesses acquire and run their forklift truck fleet on the basis of sourcing the product and maintenance support directly from an Original Equipment Manufacturer (OEM), expecting to get the best possible deal with the least exposure to risk. But, does this approach really offer the value, versatility and operational resilience businesses need today? With the right-sized deal, Forklift OEMs may be able to trim their margins in order to secure factory throughput, however, this reveals the core aim of the manufacturer – to maximise truck sales and keep the factory busy. The focus is not necessarily on providing the best possible outcome for the customer and can result in some equipment being specified that is not the most appropriate for the task, but 12
Bulk Solids Today
simply the nearest available option in the manufacturer’s product range. With incessant pressure on businesses to run leaner and more efficient warehouse and factory operations, the emphasis for most companies is now firmly on getting the most from the forklift fleet in terms of versatility to cover several tasks, flexibility to respond to changing customer demands, along with greater overall performance and reliability. In some instances, this may require specialist handling equipment that is suited to flexing across applications such as unloading or loading vehicles as well as operating in narrow aisle racking – one
BULK MATERIALS HANDLING vehicle for both purposes can save significant costs. But is an OEM likely to rush to suggest this option when the opportunity is there for additional sales? Peaks and promotions are gaining in strength and frequency, so ensuring vehicle uptime and resource availability is of prime importance to a broad range of businesses – flexibility to hire in trucks at peak periods can help trim overall fleet costs and provide extra cover when needed. Most OEMs have hire fleets, but would that option necessarily be the sales team’s first thought? Often, the best option for a business is to source according to a ‘best for purpose’ approach – this may, for example, be a telereach for loading or unloading curtain-sider trailers or an articulated narrow aisle truck that offers flexibility across duties and space saving. Few OEMs are likely to go the extra mile in procuring such a range of equipment on behalf of the customer. Particularly, if the customer is also in need of cleaning machines, access equipment, special attachments and more. So, what’s the alternative? Multi-brand material handling service and support businesses, such as Rushlift, work closely with fleet owners over the entire length of the contract to maximise the overall performance of the fleet: from specifying and recommending the most appropriate trucks for the duties to be performed – and that means providing the best truck for the job, whatever the make – to providing full, regular servicing, fast breakdown call-out, and on-site meetings to review fleet performance. From analysing the usage of individual trucks Rushlift experts can make recommendations that may save significant costs, whilst improving operational performance and reliability – maximising asset value across the lifetime of the fleet. As a national full-service provider of material handling equipment, Rushlift has service centres located strategically across the UK and over 90 highly qualified field service engineers on the road at any one time, enabling the company to provide an engineer on site within four hours (average response time to VOR). Working in-step with the customer on regular servicing maximises vehicle uptime and optimises fleet performance, building-in operational resilience across the year and, critically, at peak periods. Rigid fleet ownership models are becoming far less attractive, as businesses turn to flexible hire and leasing options which enable them to scale up or down quickly without locking up capital. Independent suppliers of materials handling equipment, like Rushlift, are in the best position to offer the responsiveness and agility businesses are now looking for through providing a best-for-purpose fleet, providing full maintenance and support, with the back-up of a large flexible hire fleet of over 300 vehicles for those busy peaks – reducing risk, increasing overall performance and providing a customer focused, best value approach. For further information on improving fleet performance, go to https://www.rushlift.co.uk
Bulk Solids Today is the bimonthly digital journal covering the storage, processing and handling of materials ranging from fine powders to the heaviest raw materials. To subscribe to Bulk Solids Today magazine or for more information, please feel free to visit www.bulksolidstoday.co.uk
High Efficiency Drying or Cooling of Bulk Solids The Bella dryer/cooler offers thermal efficiencies to 80 percent or better because air flows around material while it is suspended in the weightless zone. The result is a more consistent material.
Dynamic Air Ltd. • +44 (0)1908 622344
www.dynamicair.com Bulk Solids Today
13
BULK MATERIALS HANDLING
ADVANCING SAFETY AND PRODUCTIVITY THROUGH INNOVATION: THE DEVELON SERIES 9 EXCAVATOR RANGE
C
onstruction equipment performance has traditionally been measured by a combination of safety, productivity and operator skill. While machine design, operator competence and disciplined site behaviour remain essential, the latest generation of intelligent technologies is helping contractors achieve more on every jobsite. With innovations designed to enhance operator awareness, support accident prevention and minimise unnecessary interruptions to workflow, DEVELON’s Series 9 excavators demonstrate how safety and productivity can advance together. Today these essentials are being tested to their limits by increasing levels of jobsite complexity. Pedestrian interaction is among the most serious risks. Excavators and other heavy machines routinely work near ground personnel, other equipment and temporary structures, often with restricted space and changing traffic patterns. The consequences of a collision can be severe, which makes prevention a human priority before it becomes a commercial one. “Collisions with pedestrians are generally the most dangerous accidents,” says Stephane Dieu, Product Manager for Develon Excavators in Europe. “Given the size and weight of these machines, the consequences are often critical and can be fatal. For me, this is probably the biggest safety issue.” Safety performance is also uneven across the industry. Large contractors commonly operate detailed procedures and exclusion zones, while smaller businesses may have fewer resources and older fleets. 14
Bulk Solids Today
Rules reduce exposure, but cannot remove every unpredictable movement. THE LIMITS OF
VISIBILITY Physical machine design presents some visibility challenges that cannot be avoided. Cab improvements have helped, but it is not possible for direct visibility to cover every angle around a large, moving machine. “The behaviour of people around the machine is a major part of the problem,” says Dieu. “If nobody entered the working area, many accidents would not happen. But the operator cannot see everything on the right-hand side of an excavator, for example. “Cameras help – although rain, winter conditions or dust mean you cannot rely on a camera image alone in every situation.” The issue is whether one person can operate the machine, monitor several information sources and anticipate everyone nearby throughout a shift. Fatigue, poor
weather and distraction is likely to narrow that margin of safety. Additional sensing technology is potentially the answer; a 360-degree view combining several camera feeds, with artificial intelligence able to identify people within them. Together with radar adding distance information, these technologies can provide information that mirrors, windows or a conventional reversing camera simply cannot.
FROM WARNING TO
INTERVENTION For years, a lot of construction safety technology has been
BULK MATERIALS HANDLING passive – it presents a picture, sounds an alarm or supplies information, leaving the operator to interpret the risk and respond. While that is valuable, the direction of travel is now towards systems capable of supporting the response itself. “There is a strong influence from the automotive industry,” Dieu says. “Cars can detect another vehicle in a blind spot and, in some circumstances, stop automatically. Those technologies are progressively coming to construction equipment. “There is real demand for systems that support the operator, because even the best operator cannot be fully concentrated for eight hours every day.” An alert can be missed or delivered too late. Active intervention adds protection when a hazard reaches a defined threshold. This should not replace operator judgement or site controls, but it does offer a final opportunity to interrupt the chain that could lead to an incident. That principle can be seen in Develon’s E-Stop system, now offered on its Series 9 crawler excavators. Six high-definition cameras create a combined all-round image, with software distinguishing people from other objects. Three radar sensors provide precise distance measurement across 330 degrees around the machine, covering the principal blind-spot areas.
SAFETY WITHOUT THE
PRODUCTIVITY PENALTY The credibility of any new safety system will depend on how it behaves in the field. Frequent false alerts and unnecessary stops can disrupt cycles, frustrate operators and encourage workarounds. A technology may be technically capable yet fail in practice if it does not fit the workflow. Dieu describes Develon’s testing of E-Stop with contractors and operators in France. The most encouraging feedback, he says, was not that the system dominated the operator’s attention, but that it receded into the background
during normal operation. “After a week, the operator told us, ‘I don’t even think about it because it doesn’t disturb the way I work. I can work as usual, but I know the machine is watching and will help me if necessary,” he says. “That gives the operator more confidence and allows greater focus on the task, while still remaining responsible for safety.” A useful behavioural effect is also apparent outside the cab, as the external warning sound makes an otherwise invisible boundary very real.
THE WIDER BUSINESS CASE Preventing injury is sufficient
justification for improving safety. Nevertheless, the operational consequences of an incident explain why safety is increasingly treated as a measure of business performance. A serious accident can stop a project, damage equipment, trigger investigation and increase insurance exposure. On the flip side, a strong safety record can support prequalification and help contractors demonstrate that they can manage complex work responsibly. “Protecting people comes first, but the cost of a severe accident is also enormous,” says Dieu. “If a system prevents even one serious incident, the avoided cost can outweigh the investment across many machines. Safety technology has a real economic value as well as a human one.” The case for adoption will, of course, vary with fleet size, application and pedestrian exposure. Rental companies and large contractors may lead by standardising requirements across fleets.
TECHNOLOGY AS PART
OF SAFETY CULTURE The move towards intelligent intervention is being shaped as much by contractors as by manufacturers. Major equipment users increasingly participate in trials, set technology requirements and share evidence about how systems perform in real conditions. In France, industry-led testing of anti-collision systems has helped turn an ambition into a very practical discussion about recognition accuracy, stopping behaviour and operator acceptance. And machine specifications are now beginning to reflect that shift. Develon has made its Smart All-Around View Monitoring system, including people recognition, standard on its Series 9 excavators, while E-Stop remains an option requiring additional radar sensors and software. The distinction illustrates a likely path for the wider market: advanced visibility and detection first become expected, followed by broader adoption of intervention as confidence and demand grow. No technology can credibly promise a zero-accident site. The realistic goal is to reduce the occasions on which one missed sightline or moment of inattention leads directly to harm. That is why smart machines matter. And as prevention becomes more connected and intelligent, serious incidents can be treated less as an unavoidable feature of heavy construction – and more as events the industry has the tools and the duty to prevent. For more please visit: https:// eu.develon-ce.com/en/ Bulk Solids Today
15
BULK MATERIALS HANDLING
MORE SIFTING CAPACITY, SAME MACHINE SIZE REVOLUTIONARY PERFORATED PLATE WITH HEXAGONAL HOLE DESIGN BOOSTS THROUGHPUT
T
he Gericke Group announces the launch of a newly developed perforated plate featuring an innovative hexagonal aperture design. Engineered to maximise open area while maintaining structural integrity, this technology delivers significantly improved product throughput and process efficiency compared to conventional round-hole screens. The hexagonal geometry provides significantly more open area than an equivalent circular aperture of the same nominal size. The use of hexagonal apertures instead of conventional circular holes offers significant performance advantages in centrifugal sifting applications. Thanks to the increased open area, throughput and productivity can be substantially improved while simultaneously enhancing overall process efficiency. The optimized geometry reduces flow resistance, allowing material to pass more freely through the screen and potentially lowering energy consumption during operation. In addition, hexagonal screens can be used as a direct replacement for conventional perforated plates, making upgrades straightforward and cost-effective. THE FIGURES BEHIND THE MAGIC For an aperture size of 3 mm (across flats), a conventional circular hole (Ø 3 mm) provides an open
16
Bulk Solids Today
New hexagon type sifter screen for maximum capacity
area of 7.07 mm² per aperture, whereas a hexagonal aperture with the same nominal size offers 7.80 mm². This corresponds to a 10.3% increase in open area compared with a circular hole. Performance trials conducted with plain white flour on a GS4722 centrifugal sifter equipped with a 3 mm screen confirmed the benefits of the hexagonal design. While the circular aperture screen achieved an average throughput of 16,567 kg/h, the hexagonal aperture screen reached 19,338 kg/h, demonstrating a substantial increase in processing capacity under identical operating conditions. The hexagonal screen delivered a 14% increase in throughput, exceeding the theoretical gain in open area and demonstrating the practical process benefits of the design.
ABOUT GERICKE The Swiss Gericke Group has been designing and manufacturing equipment and systems for automated bulk material processes, as well as providing design and engineering services, for more than 130 years. Gericke bulk materials processing technology can be found throughout the world in many sectors including the food, chemical, pharmaceutical, plastics and construction material industries. Gericke’s fully owned group companies employ more than 350 experienced professionals and are located in Switzerland, Germany, Great Britain, The Netherlands, France, USA, Brazil, Singapore, Indonesia, Malaysia, Thailand and China. www.gerickegroup.com
BULK MATERIALS HANDLING
PIPE DREAMS BECOME A LIFTING REALITY WITH TURNKEY HOIST & WINCH PACKAGE
F
or a UK-based manufacturer of plastic pipe systems, flexibility is essential when handling largesection pipework and the customised angle and bend connections required by end customers. To support final assembly operations, Hoist & Winch Ltd has supplied and commissioned a turnkey package of eight aluminium mobile gantry cranes offering 2-ton safe working load (Swl), each equipped with a 110V single-phase electric chain hoist. The equipment is installed in a dedicated section of the manufacturer’s final assembly area, where pipe sections – used to protect electrical cables – are fitted with angle and bend connections. The company supplies customers across a wide range of industries, including the growing datacentre sector. Flexibility was therefore a key consideration in the specification. Manufactured by Reid Lifting, the aluminium mobile gantries supplied by Hoist & Winch feature adjustable height and span width, allowing the configuration of each crane to suit the available workspace and the dimensions of the pipes that require handling. With a maximum working hook height of 6 metres and bridge span of 4 metres, the cranes provide sufficient capacity and reach for the largest pipe sections currently processed by the company. They also offer an element of futureproofing should the manufacturer introduce larger sections. Mobility is another critical feature. Each gantry features large pneumatic-tyred wheels, making the cranes easier to manoeuvre while improving stability when travelling under load. This capability is particularly useful when moving across raised cable ramps or small floor imperfections.
The four wheels incorporate 360-degree swivel action with directional locking at 90-degree intervals, providing operators with further flexibility when positioning the gantries. Once correctly positioned over the workstation assembly jigs, manually operated heavy-duty parking brakes securely hold each crane in place. Here, the lifting systems play a vital role in the Aluminium mobile gantry cranes supplied and commissioned assembly process, by Hoist & Winch allow pipe sections, used to protect electrical safely supporting cables, to be fitted with angle and bend connections. pipe sections system, helping to maintain orderly while angle or cable routing while allowing the bend connections are fitted and hoists to travel along the bridge. adhesives are allowed to cure. Following installation, Hoist & “It’s a deceptively demanding Winch completed LOLER (Lifting application because the lifting Operations and Lifting Equipment equipment needs to combine Regulations) inspection and substantial capacity with the testing of each complete lifting freedom to move around the system and issued the appropriate assembly area,” explains Hoist LOLER Thorough Examination & Winch Director Andy Allen. reports, providing complete “The aluminium gantries give the peace of mind for the customer. customer that flexibility, while the On-site operator training 2-ton Swl hoists offer the reliable covered equipment functionality, lifting performance needed for these hoist components and operating large and varied pipe sections.” controls, including top and bottom To provide effective and limit switches and emergency-stop electrically safe lifting within the functions. Training also addressed assembly environment, Hoist & periodic checks and lubrication, Winch installed heavy-duty 2-ton together with annual inspection, Swl Yale/Loadstar 110V singleservicing and certification phase electric chain hoists. The requirements. Each operator was low-voltage supply is particularly given practical experience in using appropriate because the gantries the equipment, ensuring safe and require powering via a trailing effective operation of the new floor cable as the company moves lifting systems from day one. them between workstations. Hoist For further information and and pendant control cables are to view recent case studies visit managed across each crane bridge www.hoistandwinch.co.uk using a taut-wire festoon catenary Bulk Solids Today
17
FEEDERS & CONVEYING
BELT CLEANER POSITIONING ON HIGH VOLUME CONVEYORS R. Todd Swinderman, P.E. / President Emeritus of Martin Engineering and CEMA
A
common conveyor efficiency issue is positioning belt cleaners in the optimal locations. Structural design, spatial limitations, and safe access can be barriers to effective belt cleaning. This article will discuss primary, secondary, and tertiary belt cleaner placement. [Fig. 1] CEMA RECOMMENDATIONS ON PLACEMENT AND POSITIONING Primary cleaner placement is specified by the head pulley diameter and where the material leaves the belt. The Conveyor Equipment Manufacturers Association (CEMA) defines the secondary position as the space between the head pulley and the snub pulley on the return run of the belt. [Fig.2] Unfortunately, structural designs often result in a very short section of belt surface between the head pulley and the snub pulley, which is the ideal location for many secondary cleaner designs. This limited distance leaves little room for belt cleaners in the secondary position. Additionally, designers often place work platforms based on major components, overlooking access for belt cleaner inspection or maintenance. Belt cleaners typically require more attention than major components to ensure system efficiency because the blades are wear components that must be maintained at optimal cleaning pressures.
18
Bulk Solids Today
Figure 1 – The SQC2S™ Orion Secondary Cleaner is designed to dislodge adhered fines that create dust on the belt return.
Figure 2 – Proper placement depends on several factors, with the main being the pulley diameter.
DESIGN AND INSTALLATION CONSIDERATIONS There are many simple options designers should consider: 1. Is the drive pulley wrap angle really needed or are you just applying it from habit? A
common default wrap is 210 degrees, created by the position of the snub pulley. The gap between the head pulley and snub pulley is an ideal location for a secondary cleaner, but the combination of pulley diameters and wrap angle may make
FEEDERS & CONVEYING installation and maintenance. Since all rotating components (including the main bearings) are inside the pulley, the external stub shafts need minimal space to mount to the structure. 5. Consider professionally trained installation. Belt cleaners must be mounted accurately, typically within a few millimeters, to operate optimally and reduce the risk of belt damage. Partnering with the belt cleaner supplier ensures proper installation with minimal adjustments and helps the new chute maintain a clean, professional appearance. Figure 3 – The innovative design of the Cleanscrape® cleaner hugs the pulley’s diameter, using the curvature to its advantage.
mounting a secondary cleaner difficult and maintenance nearly impossible. We recommend utilizing an updated engineering design program that uses either the DIN or CEMA methods for calculating accurate tension values.[Fig.3] 2. Consider using a larger diameter head pulley. Choosing a head pulley based on the minimum diameter may seem like it saves money, however, the US Mining Safety and Health Administration (MSHA) reports that up to 85% of maintenance problems are due to fugitive materials, which increase costs for cleanup, labor, and equipment replacement. A larger head pulley can allow the installation of two cleaners in the primary
position and enough snub pulley space for one or two cleaners in the secondary position, significantly reducing the amount of fugitive material. 3. Prioritize ergonomic access to the belt cleaners. Maintenance personnel can spend up to a third of their time simply accessing equipment. Designing access to seldominspected or -maintained components based on minimum walkway codes increases costs. Consider structures and work platforms that facilitate belt cleaner inspection and maintenance [Fig.4] 4. Consider using motorized drive pulleys. Motorized pulleys offer energy advantages and weight savings and open up space for belt cleaner
Figure 4 – Safe & ergonomic access for maintenance is essential for retaining efficient production and consistent uptime.
CONCLUSION A belt cleaner system should be properly specified, designed, and installed to gain the direct and indirect long-term cost benefits of reduced fugitive material, but compliance is also an issue. Safe access with adequate space for installation, maintenance, and inspection is critical to supporting longer system life and a lower cost of operation. Martin Engineering is a global leader in bulk materials handling solutions. For over 80 years, Martin has designed, manufactured and installed innovative products that make the world’s foundation industries cleaner, safer, and more productive. Based in the USA, the privately owned company has drawn on its unrivalled experience and expertise to help operations improve safety, enhance material flow, reduce spillage and dust, and minimize downtime. With factoryowned facilities in 20 countries, on-theground presence in another 40, and a worldwide service partner network, Martin has built an enviable reputation for high performance products delivered with exceptional technical service and support. The company’s comprehensive Foundations™ textbooks, learning resources, and training programs are the global standard for the efficient and effective design, operation, and maintenance of bulk materials handling equipment. For more information visit martin-eng.com, email info@martineng.com, or call +1 800.544.2947. All images Copyright © Martin Engineering 2026. US and corresponding foreign patents issued and pending. ® Registered trademark of Martin Engineering Company in the US and other select locations. © 2026 Martin Engineering Company. All rights reserved. Additional information can be obtained at www.martin-eng.com/trademarks.
Bulk Solids Today
19
FEEDERS & CONVEYING
FEEDING SOLUTION FOR DIFFICULT POWDERS
A
ccurate dosing of fine powders can be challenging when materials are prone to binding, compaction and inconsistent flow. Trantec Solids Handling was approached to develop a feeding solution for a cohesive powder with difficult characteristics, while meeting requirements for variable throughput, ±1% dosing accuracy and reliable dosing over 30-minute periods. Material testing is a key part of Trantec Solids Handling’s approach to developing feeding solutions. Testing the customer’s powder under operating conditions helped establish its behaviour and allowed the feeder design to be refined around the application requirements. IDENTIFYING THE MATERIAL HANDLING CHALLENGE During testing, the material was found to bind to itself and adhere to internal surfaces, including the auger, feeder body and outlet tube. Material also accumulated at the bottom of the feeder trough, forming a compacted accumulation that increased resistance around the auger and outlet. As the build-up developed, material began to bind against the moving components, producing a grinding noise and affecting material flow. These findings highlighted the need to actively manage material flow and minimise the conditions causing build-up and binding. DEVELOPING THE FEEDING SOLUTION To address these challenges, Trantec developed a loss-in-weight screw feeder incorporating a high internal surface finish across the material-contact areas, including the feeder body, hopper, outlet tube, auger and agitator. The 20
Bulk Solids Today
smoother surfaces were designed to reduce material adhesion and retention. The auger profile was developed specifically for the application, with controlled changes to its geometry and pitch to promote smoother material movement. Both the auger and agitator incorporated designed edges to glide through the material, helping to break up bridging and maintain flow while reducing the risk of further compaction. A timed vibratory system was incorporated into the hopper. Rather than operating continuously, vibration is delivered in frequent bursts to encourage material movement without excessive agitation. This helps prevent bridging and build-up while maintaining consistent auger filling and supporting accurate dosing. DESIGNED FOR CLEANING AND CONTROLLED OPERATION Two feeders were supplied, each incorporating a quickrelease front panel for easier access to the feeding area during cleaning. This simplifies removal of residual material and helps reduce cleaning time. A control panel was supplied
to manage feeder operation and the timed vibration sequence, providing controlled and repeatable operation throughout the dosing cycle. MATERIAL TESTING AS PART OF FEEDER DEVELOPMENT The testing identified the causes of build-up and binding, allowing the auger design, surface finish, agitation and vibration system to be refined around the application requirements. If you are experiencing challenges with powder flow, or accurate dosing, Trantec Solids Handling can provide material testing and applicationspecific feeding solutions. To discuss your requirements, contact sales@trantec.net or visit www.trantec.net.
PORTS & TERMINALS
AS UK EXPORT GROWTH SLOWS, EXPERT HIGHLIGHTS THE EVOLVING ROLE OF SHIPPING CONTAINERS
S
eventy years after a converted oil tanker carried the first standardised steel boxes from New Jersey to Texas, the shipping container remains the basic unit that global trade is built on. A recent Financial Times feature examined how that system, having driven down the cost of moving goods to a small fraction of what it once was, is now running into pressure from port congestion and a widening gap between the volume of goods arriving in the West and the amount travelling back the other way. The latest data from the Office for National Statistics shows UK goods exports fell by 2.1% across 2025 which prompted William Bain, Head of Trade Policy at the British Chambers of Commerce to warn about the uncertainty for UK trade prospects, earlier this year. Cleveland Containers, part of Cleveland Group, a leading UK supplier of shipping containers and container conversions, works with businesses across the country that depend on the same network to move goods, materials and equipment. Here, they offer their insights on the changing shape of global trade and the role of shipping containers in a new era. Shipping containers changed more than the mechanics of shipping when they were standardised in the 1960s. It also determined which countries could realistically compete for manufacturing and export work, by making it cheap enough to move goods across oceans that distance stopped being a barrier. “That shift is part of the reason why the current slowdown in UK exports matters so much,” said Andrew Thompson, CEO at Cleveland Containers. “Freight rates, longer transit times and rising insurance costs all add friction to getting goods out of the country, and that lands hardest on exporters who are already competing on tight margins.” The British Chambers of Commerce has referenced Office for Budget Responsibility forecasts pointing to cooler export growth this year, following a decline in goods exports across 2025. Thompson argues that businesses reliant on shipping should expect this kind of volatility to continue. “Global shipping has been through several years of disruption now, from Red Sea rerouting to capacity being tied up elsewhere,” he said. “Exporters who build flexibility into how they source containers and plan shipments are likely to cope with that volatility better.” The pressure on exporters is matched by pressure on the ports handling the goods. DP World’s expansion of London Gateway, which will add two new berths capable of taking the world’s largest container ships, is expected to make it Britain’s largest container port within five years of the project’s approval. Similar investment has been under way
elsewhere, with the British Ports Association tracking hundreds of millions of pounds committed across ports including Belfast, Liverpool and Leith. “Ports were not built with today’s ship sizes in mind, so expansion has become a permanent feature of the industry,” said Thompson. “For businesses, that means paying attention to which ports are investing and which routes are under strain, because that increasingly determines lead times as much as the shipping schedule itself.” It’s estimated that around 1.8 million 20ft containers sit idle at any given time, roughly equivalent to the carrying capacity of the world’s eighth largest shipping line. That build-up of empty containers can leave vessels queuing for berth space to unload, adding to both the cost and the time it takes to move goods, and leaving ports themselves carrying much of that burden. Repurposing surplus containers rather than leaving them stacked at port is one way the industry can ease that pressure while giving retired stock a useful second life. Small Business UK reported that UK self-storage space using containers grew by more than 7% in the past year, with firms using them for overspill warehousing, secure on-site stores and temporary workspaces. “A container coming off a shipping route still has plenty of useful life left in it,” said Thompson. “We convert containers into offices, canteens, workshops and self-storage units for customers across construction, agriculture, retail and education, and demand for that kind of flexible space keeps growing. It’s a practical way for the industry to get more value out of stock that would otherwise sit unused while the wider shipping network works through its own problems.” Global trade may look different over the next fifty years, but the steel box that helped build it has now become part of the operational backbone of UK business. www.clevelandcontainers.co.uk Bulk Solids Today
21
PACKAGING
ERIEZ SHOWCASE ADVANCED INSPECTION TECHNOLOGIES AT PACK EXPO 2026
E
riez highlighted advanced inspection technologies at PACK EXPO International 2026, Oct. 18–21, at McCormick Place in Chicago. Visitors to Booth S-3954 in the South Hall saw live equipment demonstrations and met with product specialists to discuss contaminant detection, product quality, and production efficiency. Featured technologies included the PrecisionGuard™ X8 Metal Detector, the new X8-SF Simultaneous Frequency Metal Detector, the SenseGuard™ X-ray Inspection System, and an Eriez Recirculating Inspection System. The PrecisionGuard X8 Metal Detector combines high sensitivity with intuitive operation to detect ferrous, nonferrous, and stainless steel contaminants. Its large touchscreen interface, automated product learning, and integrated data-capture capabilities simplify operation and reporting, while its rugged design supports demanding food processing environments. The X8 is available as a standalone detector or as part of a conveyorized inspection system. The X8-SF expands the PrecisionGuard X8 platform with simultaneous frequency technology that inspects products at multiple frequencies at once. It is designed for wet, salty, and conductive foods that can challenge conventional metal detectors. The X8-SF also features a robust construction, easy-to-use touchscreen interface, and integrated data-capture capabilities. The SenseGuard X-ray Inspection System detects contaminants, foreign objects, and irregularities such as glass, stone, bone, or dense plastic materials in product lines. X-ray detectors can inspect incoming 22
Bulk Solids Today
material feeds or already packaged items, benefiting the entire downstream process. Attendees also saw the Eriez Recirculating Inspection System in operation. With vibratory feeders connected to metal detectors in a continuous loop, the system demonstrates how processors can use Eriez equipment to verify inspection results, manage rejected products, and maintain throughput without interrupting production. “Food processors need inspection solutions that reflect the realities of their production environments, from challenging product characteristics to the need for consistent throughput and clear documentation,” said Emmett Keim, Global Product Manager, Inspection Systems, Eriez. “At PACK EXPO International, we demonstrated how our inspection technologies can help processors strengthen contaminant control systems while supporting efficient day-to-day operations.” To learn more about Eriez’ advanced Magnetic Separators, Metal Detectors, X-ray Inspection Systems, and Vibratory Feeders and Conveyors for food processing and
packaging applications, visit eriez. com/Industries/Food-PackagingProcessing. Established in 1942, Eriez is a global leader in separation technologies. Our commitment to innovation has positioned us as a driving market force in several key technology areas, including magnetic separation, flotation, metal detection, X-ray inspection, and material handling equipment. The company’s 1,000+ employees are dedicated to providing trusted technical solutions to the mining, food, recycling, packaging, aggregate, and other processing industries. Headquartered in Erie, Pennsylvania, USA, Eriez designs, manufactures, and markets on six continents through 12 wholly owned international subsidiaries and an extensive sales representative network. For more information, visit www.eriez.com.
PACKAGING
COMPASS WIRE CLOTH EXHIBIT HIGH-PERFORMANCE SCREENING SOLUTIONS AT PACK EXPO 2026
C
ompass Wire Cloth, a North American leading manufacturer of separation, sifting, and screening solutions, exhibited at PACK EXPO International, October 18–21, 2026, in Chicago, IL, presenting screening products for the packaging industry designed to improve efficiency, uptime, and product quality. During the event, Compass Wire Cloth featured its Round Vibratory Screening Units and Round and Pretensioned Separator Screens. Compass Round Vibratory Screening Units deliver OEMlevel screening performance while helping reduce total cost of ownership through competitive pricing, efficient operation, and long
service life. Designed for accurate separation of both dry and wet materials in demanding industrial environments, these units provide precise particle classification and reliable removal of oversize contaminants to support consistent product quality. Optimized vibration and controlled material flow enable higher throughput without sacrificing accuracy. The Compass Round and Pretensioned Separator Screens are manufactured to fit OEM equipment and all round vibratory screeners, offering processors a dependable replacement option for a wide range of applications. Produced in a temperaturecontrolled environment, these screens are engineered for consistent
tension across the screen surface, which supports screening accuracy, longer screen life, and efficient separation of solids from liquids or classification of dry materials. For more information about Compass Wire Cloth, visit compasswire.com.
Register now to receive your digital issue of Bulk Solids Today
bulksolidstoday.co.uk/subscribe BST half page.indd 1
01/07/2026 Bulk Solids13:30:55 Today
23
PACKAGING
SUN AUTOMATION GROUP® AND ELITRON AMERICA ANNOUNCE STRATEGIC NORTH AMERICAN SALES PARTNERSHIP SUN Automation to Represent Elitron’s Digital Cutting and Automation Solutions Across the U.S., Canada and Mexico
S
UN Automation Group®, a provider of innovative machinery, technology and support solutions for the corrugated industry have announced a strategic partnership with Elitron America, an Italian manufacturer of digital cutting and automation systems. Under the agreement, SUN Automation will represent Elitron throughout the United States, Canada and Mexico, bringing Elitron’s digital cutting and automation solutions to more box makers across North America. Since opening its Norcross, Georgia office in 2017, Elitron has continued to build its North American presence through a growing corrugated install base and local sales and technical support. “With SUN Automation, we now reach more box makers through a name they already trust,” said Daniele Gallucci, President of 24
Bulk Solids Today
Elitron America Inc. “What they get is a system built for corrugated, not adapted to it. That difference shows up on the floor every day.” Elitron develops automated digital cutting systems for corrugated packaging, displays and industrial applications. Its KOMBO line ranges from standalone cutters to fully automatic pallet-to-pallet systems with automatic pallet swap, built around patented Elitron technologies including the Seeker System vision platform and AiroPanel unloading. Over 100 fully automatic KOMBO TAV systems are installed worldwide. “We heard strong feedback from customers already using Elitron equipment, and that gave us confidence in both the company and the reliability of its technology,” said Gokul Gopakumar, Vice President of Technology and Business Development at SUN Automation Group. “The level of automation they bring was also important to
us because it aligns with what we’re seeing customers look for across the corrugated industry.” For SUN Automation, Elitron represented an opportunity to add digital cutting to its broader corrugated offering. The technology complements SUN Automation’s existing equipment and partner solutions and expands the range of production challenges the company can help customers address. “Our customers are looking at the entire production operation and asking where new capabilities can create value,” said Greg Jones, Executive Vice President at SUN Automation Group. “Elitron broadens the range of solutions SUN Automation can bring to the market and strengthens our ability to support customers as their production needs evolve.” To learn more about SUN Automation Group, visit: sunautomation.com. To learn more about Elitron, visit: elitron.com.
PACKAGING
AKONA PROCESS SOLUTIONS RETURNED TO PPMA WITH COMPLETE POWDER HANDLING EXPERTISE
L
eading material processing and handling solutions company, Akona Process Solutions returned to the PPMA Show 2026 bringing together the expertise of its four specialist brands - Cablevey, Kason, Marion and Spiroflow - to demonstrate complete powder handling and material processing solutions for manufacturers across multiple industries. Exhibiting on Stand B76, Akona showcased a carefully selected range of equipment that highlighted the breadth of its process capabilities, from raw material delivery through conveying, screening and mixing. Visitors were able to see equipment first-hand from across the Akona portfolio, including a Cablevey tubular drag conveyor, Kason Centri-Sifter centrifugal screener, Spiroflow flexible screw conveyor and sack tip station, plus a Marion horizontal mixer. Together, the technologies demonstrated how manufacturers can create
efficient, integrated material handling systems that improve product quality, minimise waste and increase production efficiency. Serving customers across the food, beverage, pharmaceutical, chemical, minerals and pet food industries, Akona combines the engineering expertise of four respected brands under one organisation, providing customers with a single source for complete powder processing solutions. Throughout the exhibition, experienced application engineers and sales specialists were available to discuss individual manufacturing challenges and recommend integrated solutions tailored to specific production requirements. Whether manufacturers are upgrading existing equipment, expanding production capacity or designing new processing lines, the team could advise on technologies that improve reliability, consistency and operational performance. By bringing together conveying, screening, mixing, bulk material
handling and process automation expertise, Akona is uniquely positioned to support manufacturers looking to simplify supplier management while benefiting from proven equipment across every stage of the production process. Tom Finnegan, Akona’s director of sales EMEA, said: “We were delighted to return to PPMA and to meet customers old and new. The exhibition provided an ideal opportunity to demonstrate the strength of our combined portfolio and show how our four specialist brands work together to deliver complete process solutions. “Visitors increasingly want more than individual pieces of equipment - they’re looking for integrated systems backed by genuine application expertise. That’s exactly what our team will demonstrated throughout the show, helping manufacturers improve efficiency, product quality and longterm production performance.” Visit Akona here to find out more. akonasolutions.com/en-gb/
Bulk Solids Today
25
PACKAGING
BONFIGLIOLI’S MECHATRONIC SOLUTIONS AT PARCEL+POST EXPO 2026
B
onfiglioli participated at Parcel+Post Expo 2026, the leading global event for the postal, parcel and eCommerce logistics industry in London on 23 - 24 September. At the exhibition, the company showcased its latest automation and drive solutions, designed to improve efficiency, reliability and sustainability across parcel handling and logistics operations. As a trusted global partner for OEMs developing machinery, automation systems and technologies for sorting and material handling applications, Bonfiglioli combines a comprehensive portfolio of high-performance solutions with worldwide service and technical support. HIGH-DYNAMIC SOLUTIONS FOR AGV FORKLIFTS AND AMRS Among the highlights on display was the BMD Series three-phase synchronous motor, a compact, low-voltage solution designed for high-dynamic industrial applications.
26
Bulk Solids Today
Featuring low-to-medium inertia and permanent magnet brushless technology, the BMD operates at 24 - 48 V and combines the benefits of low-voltage operation with the superior performance of a three-phase AC motor. Compared with conventional DC stepper motors, it delivers higher efficiency together with outstanding torque and dynamic response. The BMD Series is particularly well suited to the evolving material handling sector, where fixed conveyor systems are increasingly being replaced by autonomous and mobile solutions. At Parcel+Post Expo, the motor was showcased in combination with a planetary gear unit of the MP Series. The MP series further enhances the solution with its modular design, wide range of gear ratios, multiple backlash classes and optimized lubrication options, ensuring maximum flexibility across a variety of applications. Autonomous Mobile Robots (AMRs) are playing an increasingly important role in optimizing intralogistics processes by enabling
flexible, efficient and autonomous material transport. To address the growing demand for highperformance mobile platforms, Bonfiglioli showcased a compact low voltage wheel-mounted planetary gearmotor of the BMS Series. Specifically developed for AMRs, the BMS Series combines permanent magnet technology with a low-voltage synchronous threephase AC motor in a compact, flange-free design that delivers high torsional stiffness, low moment of inertia and excellent positioning accuracy. The result is a highly efficient, space-saving solution that provides the dynamic performance, reliability and flexibility required by next-generation autonomous material handling systems. INTEGRATED DRIVE SOLUTION FOR COMPACT WAREHOUSE The BMD brushless motor is also present in a solution developed for compact warehouse elevator axes, coupled with the a parallel shaft gearbox of the F Series.
PACKAGING Together they build a compact, high-performance drive package specifically designed for spaceconstrained applications. Its compact footprint makes it ideal for vertical storage systems, where high dynamic performance, precision and reliability are essential for the rapid movement of drawer-based modules used to store components and materials. The solution is further enhanced by the AxiaVert drive, enabling Bonfiglioli to supply a complete drive package that also integrates advanced functional safety features. This is particularly important in vertical warehouse applications, where operators frequently interact with the system during loading and unloading operations, requiring the highest levels of safety in shared working areas. ENGINEERING BEYOND STANDARD: CUSTOM DRIVE SOLUTIONS BY BONFIGLIOLI At Parcel+Post Expo, the company showcased two customengineered drive solutions, highlighting its capacity to design application-specific systems. The first solution combines a custom parallel shaft gearbox with a compact, high-efficiency permanent magnet motor in a fully integrated package, delivering exceptional compactness together with the dynamic performance required by a wide variety of material handling applications, including shuttles, vertical storage systems and lifting equipment. Alongside it, Bonfiglioli presented a compact drive solution based on a helical bevel gearbox combined with a compact synchronous brushless motor. Designed for transport, conveying and general automation applications, the integrated solution offers a remarkably compact footprint while extending the available operating speed range beyond that of conventional geared motors, making it particularly suitable for highly dynamic and intermittent-duty cycles.
THE COMPLETE AXIA DRIVE FAMILY FOR MODERN AUTOMATION For Bonfiglioli, Parcel+Post Expo was the ideal stage to showcase the Axia family full product range, featuring AxiaVert and AxiaAgile. The former is tailored for highperformance and complex systems, featuring a modular design, comprehensive functional safety options and advanced motion control capabilities. The latter offers a compact and cost-efficient alternative for general-purpose uses. Built on a variant-based concept, AxiaAgile is engineered to address diverse application requirements, providing dedicated configurations that streamline product selection and significantly reduce engineering time. Available in three functional safety variants - Basic, Standard and Motion - AxiaVert provides the flexibility required to adapt to different application scenarios. This represents a key advantage, enabling optimized safety architectures, reduced footprint, and eliminating the need for external safety components, while ensuring safe and controlled operation across multiple movements. EVOX: CONFIGURATION FLEXIBILITY, GLOBAL COMPATIBILITY, AND SUPERIOR PERFORMANCE Present at Parcel+Post Expo 2026, Bonfiglioli’s EVOX gearmotor is designed for conveyor and material handling applications. Available in a wide range of configurations, EVOX offers a compact design and installation flexibility. Another feature is the new dynamic brake, developed for high-cycle applications typical of the postal and parcel handling industries. This is complemented by the universal brake power supply, making the motor suitable for global markets. Combined with an extensive portfolio of international certifications, this enhancement enables OEMs and end users to standardize a single motor platform
worldwide, reducing inventory complexity and simplifying machine design. Additional new features include an orientable terminal box for easier wiring across different machine layouts. It is paired with Bonfiglioli’s high-efficiency helical bevel gearbox which offers reduced installation space, wide output speed range, high stiffness for dynamic application and safe operation in potentially explosive atmospheres. BONFIGLIOLI IIOT SOLUTIONS FOR SMARTER AND MORE EFFICIENT OPERATION Extending operating time while reducing maintenance costs is a key priority for today’s industrial machinery manufacturers and operators. To support these goals, Bonfiglioli offers advanced Industrial IoT (IIoT) solutions that combine Condition Monitoring and Predictive Maintenance, helping customers improve machine reliability and operational efficiency. Through its proprietary IoT platform and dedicated sensors, Bonfiglioli continuously monitors the health and performance of gearboxes and motors, collecting real-time data on operating conditions and energy consumption. By identifying potential issues before they lead to failures, the system enables predictive maintenance strategies that reduce unplanned downtime, optimize service scheduling and extend equipment lifetime, giving users greater visibility and control over their operations. Bonfiglioli’s presence at Parcel+Post Expo marked an important step in consolidating its role in the parcel and postal automation sector. Thanks to its extensive manufacturing and distribution network, together with a high degree of product customization, from mechanical interfaces to firmware, software and IoT integration, Bonfiglioli is able to meet the evolving needs of customers across international markets. www.bonfiglioli.com.
Bulk Solids Today
27
PACKAGING
ENDOLINE CUSTOMERS GET ENTERPRISING WITH MES Rolling out a Manufacturing Execution System (MES), which tracks and manages production on the factory floor, and connecting it with enterprise-level ERP platforms that manage business functions such as orders, stock and planning, can fundamentally transform operational capabilities.
H
aving a unified approach also enables comprehensive batch traceability, offering manufacturers greater oversight and control throughout their production processes. While the concept of transitioning to integrated systems and establishing two-way data sharing between systems can appear somewhat futuristic, with the appropriate support and a well-defined strategy, the process is straightforward. Andrew Yates, Managing Director of Endoline Automation and Endoline Robotics, explores the implementation steps UK food and beverage processors need to consider. TRACKING THE ORDER TO PALLET PIPELINE By integrating Endoline robotic packaging and palletising machinery with customised MES reporting tools, manufacturers can connect directly into SAP and other enterprise resource planning (ERP) platforms. Linking business planning to shop floor operations, this integrated setup eliminates 28
Bulk Solids Today
Endoline Robotics' integrated palletising systems can communicate directly with ERP and MES platforms, giving manufacturers real-time visibility of production, improving traceability and automating the flow of data from order through to pallet.
data silos, reducing inefficiencies, miscommunication and errors, resulting in a smoother workflow. Although there may be a strong impulse to integrate MES software and automation hardware simultaneously, Endoline usually recommends a phased approach. “This will typically depend on the scale of the installation project. But we would often suggest delaying full ERP/MES programming until the physical hardware is operational,” confirms Andrew. The reason, he explains, is to
ensure the high-speed packing and palletising lines have been fully tested and validated. “It never takes long for our in-house specialists to roll out the MES coding once the boxes start moving. Taking this approach ensures that the digital systems are fully aligned with how the production line actually operates,” Andrew explains. OPTIMISING PRODUCTION SCHEDULING The extraction of data can be as complex or as simple as
PACKAGING processors want. Smart factories are increasingly adopting a central data system (often called a Unified Namespace or UNS), enabling both MES and ERP systems to share data efficiently. Having this standardised connectivity makes it easier to scale up the use of production data. For ease, many utilise OPC-UA and RJ45 Ethernet interfaces, as these formats enable manufacturers to extract detailed, real-time data from most machines. For example, checkweigher systems can calculate rejection versus acceptance rates in real time, while case packing robots can report the exact volume in every box and the count of boxes stacked on a pallet. Additionally, there are tools that can generate sustainability metrics, enabling managers to monitor energy use and air consumption in real time. “Endoline develops our middleware in-house. This helps customers as it is designed specifically to support our equipment. It also enables a food processor or packing operation to easily move from manual processes to more advanced, multi-line automated palletising as the business grows,” highlights Andrew. ACCURACY AND ALIGNMENT The availability of detailed, real-time data fundamentally changes the landscape for supply chain planning. With the integration of MES and ERP systems, the entire production
and packing process becomes more streamlined and efficient. For example, manual tasks such as interpreting production requirements or sending instructions through paper-based methods are eliminated. Instead, the ERP system automatically communicates requirements to the MES, which then instantly sends clear instructions to the robotic systems on the shop floor. This automation reduces the need for human intervention and ensures that information flows smoothly across all operational departments. The ability to deliver production instructions immediately and without error is especially crucial for food safety and traceability. “An integrated approach ensures that instructions are shared accurately and efficiently from business systems to shop floor robotics. By aligning production activity with wider business goals, manufacturers can minimise mistakes, improve efficiency and maintain consistent product quality,” explains Andrew. DECENTRALISING DATA AT LIFE HEALTH FOODS This was the cross-departmental data model adopted by Life Health Foods. From 11 cereal packing lines, product cases are labelled by one of eight GS1compliant print-and-apply label systems. Using Endoline’s ERP software, all label and case information is automatically fed into the company’s SAP system.
The result is a “single source of truth” where automated sorting sensors know exactly what is in every box, when it was produced and where it needs to go, all without any human intervention. The ERP reporting system plays a critical role in supporting the management of multiple SKUs for the UK cereal manufacturer. Realtime visibility enables immediate identification of any quality or stock issues that may arise during production. This proactive approach ensures that potential packing or palletising bottlenecks are detected and addressed before they escalate into significant problems. As a result, Life Health Foods is able to maintain a smooth production flow, minimise disruptions and uphold consistently high standards across all product lines. “Processors that are moving towards a centralised data-sharing approach and two-way data flow between systems are reporting significant benefits,” adds Andrew. The central data model (UNS) in particular represents a shift away from rigid system connections, allowing systems to access and share data more flexibly. For further information on any of Endoline’s extensive range of machines, please contact Endoline Robotics on Tel: + 44 (0) 1767 310581 email: sales@ endoline-automation.com or visit the website at www.endolineautomation.com.
Bulk Solids Today is the bi-monthly digital journal covering the storage, processing and handling of materials ranging from fine powders to the heaviest raw materials. To subscribe to Bulk Solids Today magazine or for more information, please feel free to visit www.bulksolidstoday.co.uk
Bulk Solids Today
29
BUYERS GUIDE Aero Mechanical Conveyors
Conveyors & Elevators
Powder Handling Systems
“Often copied NEVER matched”
Suppliers of the Original Entecon® Aero Mechanical Conveyors Other Products: • Sack Openers • FIBC Fill / Discharge Tip or Automatic • Pneumatic Conveyors
Sales office for UK & ROI: SGH Equipment - Entecon® Agent
Tel / Fax: 01270 651611
E: sales@sghequipment.co.uk • www.sghequipment.co.uk
Bulk Storage & Handling
MANUFACTURERS OF SILOS, TANKS AND CONVEYING SYSTEMS Redbrook, Barnsley S75 1HR Tel: 01226 730037 Fax: 01226 730066 Email: info@eb-equipment.com Web: www.eb-equipment.com
6SHFLDOLVWV VLQFH LQ GHYHORSLQJ EXON PDWHULDOV SURFHVVLQJ DQG KDQGOLQJ SURMHFWV ZLWKLQ WXUQNH\ GHVLJQ DQG SODQW VROXWLRQV 'HVLJQ (QJLQHHULQJ 3URMHFW 0DQDJHPHQW %HVSRNH 0DFKLQHU\ 0DQXIDFWXUH 6LWH ,QVWDOODWLRQ &RPPLVVLRQLQJ 7XUQNH\ 6ROXWLRQV &$' $QLPDO )HHG 3HW )RRG *UDLQ 6HHG %LRPDVV +DQGOLQJ )XHO *HQHUDWLRQ :DVWH 5HF\FOLQJ +XPDQ )RRG
Bulk handling with complete confidence Designers and UK manufacturers of: • Bucket elevators • Chain & flight conveyors • Screw conveyors & bin dischargers • Belt conveyors
Remote Silo Monitoring
www.perryengineering.com Tel: 01404 891400 Fax: 01404 891402
Tuf-Lok (UK) +44 (0) 1706 822512 www.tuflok.com
*$0( (QJLQHHULQJ /WG 7HO (PDLO VDOHV#JDPH HQJLQHHULQJ FRP ZZZ JDPH HQJLQHHULQJ FRP
Cleaning
Mixers & Blenders
Dynamic Air Ltd. Milton Keynes England
+44 (0) 1908 622344 www.dynamicair.com
30
Bulk Solids Today
If you would like your company to be featured here, please get in touch using the details below : 01933 316931 bst@abbeypublishing.co.uk www.bulksolidstoday.co.uk
BUYERS GUIDE Sieves & Sifters Cont’d
Sack Filling
*OREDO 6LHYLQJ DQG )LOWUDWLRQ 6SHFLDOLVWV
Manufacturers of semi/fully automatic weighing and filling machines into valve/open mouth sacks.
7\YP[` [OYV\NO PUUV]H[PVU
T: +44 (0)1487 711114
E: enquiries@atsackfillers.co.uk www.atsackfillers.co.uk manufactured in the UK
&DOO XV RQ
ATEX
W-0729a CLASSIFIED.qxd
5/15/08
1:33 PM
Page 1
Screeners
6:(&2 (XURSH Vibratory & centrifugal Solids/solids or liquid/solids separations Standard and custom designs Industrial, food, pharm. designs
:RUOGZLGH OHDGHUV LQ YLEUDWRU\ VFUHHQLQJ DQG VHSDUDWLRQ HTXLSPHQW &RPSOLDQFH ZLWK )RRG (& 5HJXODWLRQ &RPSOLDQFH ZLWK $7(; 'LUHFWLYH (&
www.kasoneurope.co.uk
ISO 9001: 2000
W-0729a
Tel: +44 (0)1782 597540 Fax: +44 (0)1782 597549 sales@kasoneurope.co.uk
Screw Feeders, Mixers & IBC Systems
,QQRYDWLYH GHVLJQ WR JXDUDQWHH DQ HIILFLHQW UHOLDEOH DQG VDIH SURFHVV 7HO )D[ (PDLO XNVDOHV#VZHFR FRP ZZZ VZHFR FRP
Vacuum Cleaning
AJAX
Screw Feeders, Mixers & IBC Systems Ajax Equipment Ltd Tel: 01204 386723 Fax: 01204 363706 www.ajax.co.uk email: solids@ajax.co.uk
Valves
ntitled-2 1
22/10/2013 14:56:57
Posi-flate Milton Keynes England +44 (0) 1908 622366
www.posiflate.com
Intermodal dry bulk logistics for polymers, chemicals & minerals Cost effective Environmental savings Reduced C02 emissions
www.InterBulkGroup.com
InterBulk GROUP
Bulk Solids Today
31