The UK's only magazine covering the surface finishing industry
AUGUST 2026 WE HAVE EVERYTHING COVERED –
follow us on X (twitter) @surfaceworldmag – visit www.surfaceworld.com
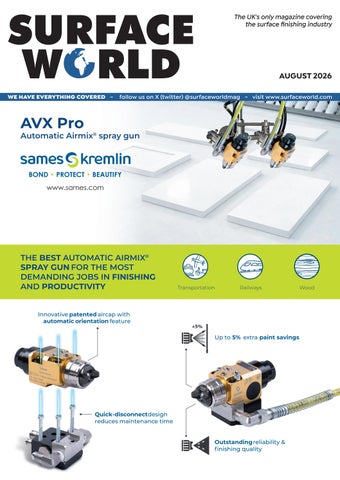
AVX Pro
Automatic Airmix® spray gun
BOND • PROTECT • BEAUTIFY www.sames.com
THE BEST AUTOMATIC AIRMIX® SPRAY GUN FOR THE MOST DEMANDING JOBS IN FINISHING AND PRODUCTIVITY
Transportation
Railways
Innovative patented aircap with automatic orientation feature Up to 5% extra paint savings
Quick-disconnectdesign reduces maintenance time Outstanding reliability & finishing quality
Wood
High pressure low volume
The Cobra 40-10 & Cobra 40-25 High-pressure double diaphragm pump: • • • •
Practically pulsation-free for high surface quality Very low detergent consumption Applications up to 250 bar and 5 l/min For aggressive, abrasive or shear-sensitive materials
go.wagner-group.com/cobra
Contact Wagner Spraytech (UK) Ltd Telephone: 01327 368410 enquiries@wagner-group.com
AUGUST 2026 VOLUME 33 NUMBER 8 MANAGING DIRECTOR & ADVERTISEMENT DIRECTOR Nigel Bean t: +44 (0) 1442 826826 e: nigelbean1@aol.com nigelbean@surfaceworld.com EDITOR & GRAPHIC DESIGNER Jane Soones e: janesoones@aol.com janesoones@surfaceworld.com CIRCULATION & SUBSCRIPTION DEPARTMENT t: +44 (0) 1442 826826 EXHIBITION ORGANISATION t: +44 (0) 1442 826826
COMPANY SPOTLIGHT THE CHROME-FREE CHEMISTRY NOBODY’S TALKING ABOUT.
2
QUALICOAT UK & IRELAND QUALICOAT UK & IRELAND AWARDS SEASIDE LICENCE TO KESTREL POWDER COATING.
6
INSTITUTE OF MATERIALS FINISHING INDUSTRY RECOGNISED TRAINING COURSES FROM THE IMF.
10
INDUSTRY NEWS Hill Media Ltd, Marash House 2-5 Brook Street, Tring, Hertfordshire HP23 5ED, United Kingdom. The Surface World magazine is published 12 times a year by Hill Media Ltd. Although every effort is made to ensure the accuracy and reliability of material published in Surface World, Hill Media Ltd and its agents accept no responsibility for the veracity of claims made by contributors, manufacturers or advertisers. Copyright in all material published in Surface World, including but not limited to all Hill Media brands, brand logos, trademarks, and associated assets, remains with Hill Media Ltd and its agents. © Hill Media Ltd – 2026 ISSN 1757-367X
DFT INSTRUMENTS BECOMES UK DEFELSKO AUTHORISED SERVICE CENTRE.
12
AVX PRO, THE NEW AIRMIX STANDARD FOR INDUSTRIAL PRODUCTION LINES.
14
WITHAM GROUP ANNOUNCES TWO NEW BOARD APPOINTMENTS TO DRIVE STRATEGIC GROWTH.
18
A LEADING PLATFORM TO EXHIBIT.
20
®
AEROSPACE & MARINE CORROSION PREVENTION IN AEROSPACE AND MARINE ELECTRICAL SYSTEMS.
24
ELECTROPLATING, ANODISING & GALVANIZING
NO ROOM FOR COMPROMISE.
MEDIUM-TEMPERATURE SEALING PROMISES ENERGY SAVINGS.
30
POLYPLAS ENGINEERING LTD HAVE BEEN SERVING THE FINISHING AND PLATING INDUSTRY FOR 40 YEARS.
32
PERIODIC PULSE RECTIFIERS: ENABLING STABLE TRIVALENT CHROMIUM PLATING.
36
THE BEST KEPT SECRET IN THE INDUSTRY IS JUST A LOAD OF BALLS! 38
TESTING & MEASUREMENT
QUALICOAT delivers performance, durability and compliance for architectural powder coating in the built environment.
Raise your standards. Join our global network
NEW: BYKO-SPECTRA LED 6.
40
PUMPS & FILTRATION NEW GEAR-TYPE METERING PUMP FOR PRECISE PAINT DOSING.
42
SURFACE PREPARATION, DEGREASING & CLEANING IMPORTANCE OF GOOD TOOLING.
46
STOP PAYING FOR PROBLEMS YOU COULD HAVE PREVENTED.
50
FRENCH SUPPLIER OF REFUSE COLLECTION VEHICLES PLACES HIS TRUST IN RÖSLER’S BLAST CLEANING COMPETENCE.
52
COST-EFFECTIVE SOLVENT CLEANING WITH FOCUS ON WHAT MATTERS MOST.
58
PAINT & POWDER WHY PROTECTIVE COATINGS AND FLOORING ARE FOUNDATIONAL STADIUM CONSIDERATIONS.
60
THE FARADAY CAGE: WHY “ELECTROSTATIC” SOLUTIONS FAIL IN RECESS COATING.
62
MATERIAL & EQUIPMENT SUPPLIERS
66
COMPANY SPOTLIGHT
THE CHROME-FREE CHEMISTRY NOBODY’S TALKING ABOUT Aerospace finishing has spent the last decade in the search for alternatives to hexavalent chromium, due to its carcinogenic properties which are tightly regulated, and increasingly unwelcome on customer specs. What has received far less attention is the role water quality plays in keeping these alternative processes within specification. Ionic contaminants introduced through make-up or rinse water can accumulate in anodising and sealing baths, affecting coating formation, corrosion resistance and paint adhesion. In an aerospace environment, the consequence can be failed acceptance testing, rework and costly line downtime.
Take Tartaric Sulphuric Anodising (TSA),
On paper it’s a straightforward swap.
now the front-runner replacing chromic
In practice, the interaction between
acid anodising across much of the
tartaric and sulphuric acid brings different
supply chain.
wastewater management requirements whereby TSA effluent must be segregated from other metal-bearing waste streams for the prevention of complexing of other metals. This is the bit that tends to get skipped in the “why water purity matters” conversation: it’s not really about clean water in the abstract. It’s about the fact that regulatory pressure has pushed the industry toward chemistries that are structurally more sensitive to what’s in your rinse tanks, right at the moment when margin for error has shrunk. AllWater Technologies ran into exactly this when a specialised aerospace engineering firm, Aero Fabrications, needed to bring a new TSA and Boric line online to support its growth. The anodising chemistry itself was only half the brief.
2
YOU MAY A NOT SEE IT. AY
T NCE TEST W TA YOUR R ACCEPTA WILL.
Contaminants don’t just stay in the rinse tank. MAKE WATER PART OF THE SPEC. Talk to AllWater before your next finishing line goes live.
20+ Aerospace & Defence Capital Projects +44 (0)1934 751333 · enquiries@allwatertech.co.uk · allwatertreatment.co.uk
COMPANY SPOTLIGHT
AllWater built a reverse osmosis plant to provide process compliant water for make-up and rinsing, then paired it with a dedicated treatment system for the effluent, including stream segregation and removal of tartaric acid. The completed system provides consistent, process-compliant water for make-up and rinsing across Aero Fabrications’ TSA and boric sulphuric anodising processes. Together with the segregated wastewater treatment system, it supports the company’s expanded aerospace finishing capability. These projects demonstrate the water quality, rinse strategy and effluent management must be considered as integral parts of the process – not simply as supporting utilities.
Across more than 20 capital projects for aerospace and defence manufacturers, AllWater has delivered high-purity water and wastewater treatment systems,
including multiple water recovery plants designed to reduce consumption and discharge volumes. The lesson for anyone specifying a new line isn’t “buy the purest water available.” Both water quality and the way it is used, including the design and control of rinsing stages needs to be considered alongside the process chemistry from the outset. The industry’s move away from chrome has quietly made water the variable most likely to catch you out. Anodisers evaluating a TSA or other chrome-free conversion would do well to ask their water treatment partner the same question they’re asking their chemical supplier: what happens when the input isn’t perfectly consistent? AllWater Technologies designs and supports high-purity water and wastewater treatment systems for aerospace and defence manufacturers across the UK. Telephone: +44 1934 751333 Email: enquiries@allwatertech.co.uk Visit: www.allwatertreatment.co.uk
4
at im cl ns
itio nd
co | e
c rfa
su
It’s not just the Elcometer 456 Coating Thickness Gauge that’s fast...
ic
Coatings Inspection Equipment
ss
e in nl
ea cl
Generate professional inspection reports in seconds using the FREE ElcoMaster® Data Management Software.
| at
co g in k ic
th ss
ne ity
os
n
io
rfa
ce
su Surface World - Ella.indd 2
pr
o
file
|a
d
s he
|
n
pi
e
l ho
&
r po
INSPECT IT
elcometer.com 12/05/2025 07:45:13
Contact us www.unitechshyre.co.uk 01543 224531 info@unitechshyre.co.uk
QUALICOAT UK & IRELAND
QUALICOAT UK & IRELAND AWARDS SEASIDE LICENCE TO KESTREL POWDER COATING QUALICOAT UK & Ireland has officially awarded its prestigious Seaside licence to long-standing member, Kestrel Powder Coating. While standard QUALICOAT licensing provides quality assurance across the entire powder coating process, the Seaside specification is engineered for more challenging, exposed locations. The key technical requirement of the Seaside specification is that the system passes additional corrosion testing; in order to achieve this the applicator must
6
increase their etch to achieve at least double the standard QUALICOAT requirement of 1g/sm of metal removal from the aluminium surface during pretreatment. The Seaside specification requirement removes more surface contaminants and therefore creates a more robust pretreatment for areas where atmospheres carry corrosive salts and other aggressive pollutants.
Chris Mansfield QUALICOAT UK & Ireland Chair
QUALICOAT UK & IRELAND
operational standards. Attaining the Seaside classification is a significant milestone that provides customers with complete assurance that Kestrel’s finishes meet the highest standards available and can withstand the toughest conditions.” QUALICOAT UK & Ireland strongly advises specifiers, architects and fabricators to specify Seaside class powder coating for any projects located within 5km of the coast and tidal estuaries.
To secure the licence, Kestrel proved
“We are pleased to award Kestrel
through strict processes and monitoring
Powder Coating the Seaside specification
that it consistently achieves the 2g/sm
licence,” comments Chair of QUALICOAT
etch rate, and produced coated samples
UK & Ireland Chris Mansfield. “As an
that passed the additional, independent
established member, Kestrel has
testing.
continuously demonstrated high
Contact Seaside accredited powder coaters via the QUALICOAT UK & Ireland website: qualicoatuki.org/coating where certified coaters are highlighted in grey. The accreditation can also be verified using the QR code on the licensee’s QUALICOAT certificate.
Powder Checker
Non-contact Uncured Powder Thickness Gauge Affordably measures uncured powder coatings using non-contact ultrasonic technology to predict a cured thickness
Dedicated stand-alone unit is ready to measure right out of the box
Fast measurement speed—ideal for moving lines and swinging parts
Scan Mode continuously takes measurements—ideal for analyzing large areas
Storage of 999 readings with onscreen averaging. Stored readings can be downloaded to PosiSoft Desktop Software
Powder Inspection Kits
Complete solutions for measuring powder coating before and after cure are available 16A Long Drive, Meadway, Berkhamsted, Herts HP4 2PN t: 01442 879494 www.dftinstruments.co.uk e: sales@dftinstruments.co.uk
Kemet
Precision Lapping | Polishing | Cleaning | Materialography
Cleaning Fluids Specialist detergents available in neutral, alkaline and acid types. Kemet are a distributor of NGL cleaning fluids with more than 300 high performance formulations providing a solution to most cleaning challenges.
Vacuum Solvent Cleaning Cleans component areas that are hard to reach with modified alcohols, including blind holes and tubes. Distillation, separation, and filtration effectively removes and recovers oils and swarf particles, allowing 99% material waste recovery and minimal loss of solvent.
Passivation, FPI & Component Cleaning Systems Kemet International Ltd, Parkwood Trading Estate, Maidstone, Kent, ME15 9NJ, UK
01622 755287
cleaning@kemet.co.uk www.kemet-cleaning.co.uk
INSTITUTE OF MATERIALS FINISHING
Become an Acknowledged Leader in Surface Engineering and Materials Finishing:
INDUSTRY RECOGNISED TRAINING COURSES FROM THE IMF To follow on, students can then elect
Are you involved with the application of coatings to enhance and protect your products? Do you need to meet client specifications to ensure the longevity of your components? Does the complex world of surface engineering and materials finishing cause you headaches? If so, the courses offered by the Institute of Materials Finishing (IMF) could be your solution! The IMF have been promoting knowledge in the surface finishing industries, both inorganic surface treatments including plating and the application of organic paints, lacquers and varnishes for many years. Large numbers of engineers and technicians across a multitude of industries have benefitted from the knowledge gained to enhance their careers, their standing within industry and the ability to problem solve the many challenges they face in their daily working lives!
10
Starting with the Foundation level course, students gain knowledge on all aspects of materials finishing, specifically aimed at their own industry requirements, but to include sections on Health & Safety, the Environment and Surface Finishing and Corrosion Protection. There is no need for a science background to be able to successfully complete a foundation course. The Foundation Course requires study of 15 sections and requires the submission of 2 marked assignments followed by an end examination. The course, conducted by distance learning will take 16 weeks to complete. There are three specific study routes to choose from; electroplating, organic coatings and aerospace finishing. On successful completion, the student is awarded the Foundation Certificate.
to progress to the Technician level modules, which give more in-depth knowledge for key finishing technologies, their application and best practice methods. Again, both inorganic and organic technologies can be studied to match the industry requirements. There is a choice of eight modules, which provide study in applicable areas of surface finishing best matched to your needs. Like the Foundation course, study is by distance learning, and the student is required to complete four marked assignments and pass an examination. Passing two technician modules leads to the award of Technician Certificate; passing four modules leads to the award of an Advanced Technician Certificate.
If you feel your career could benefit from being a recognised specialist in your particular branch of Surface Engineering or Materials Finishing, then contact the IMF today. Speak with our training manager Karen Yates on +44 (0)121 622 7287 or email karen@materialsfinishing.org. Move your career to the next level and join the finishing community and all the benefits that gives through the IMF.
Solutions for Parts & Paint Spray gun cleaning
WASHERS Manual | Automatic Our high quality, advanced range of equipment provides the best way to clean paint spray guns or industrial parts. With numerous options, you can be sure that there is a model in our extensive range that meets your cleaning requirements using either solvents or water. • ATEX certified • High quality alloy pumps • Stainless steel construction • Wash cycle controlled by timer • Wash & rinse • Hot water wash • Inbuilt water recycling • Inbuilt solvent recycling • Air extraction • 2 year warranty
Working Across Aluminium Industries to Improve Your Processes
ASK FOR
A FREE
QUOTE
Specialist in the Supply of Anodising & Metal Finishing Technologies QUALICOAT Approved Chrome & Phosphate Free Technologies Low-Temperature Degreasing & Sealing Solutions
UY B OR LEASE ANODISING PRETREATMENT CONVERSION COATING
For more information visit:
www.solutex.co.uk info@solutex.co.uk | 01691 622 225
Supplied with Excellent Technical Suppor t… +4 44(0)1978 660297
info@almetron.co.uk
almetron.com
Surface Technologies l Controlled Shot Peening l Laser Peening l Keronite PEO l Thermal Spray Coatings l Dry Film Lubricants l Organic and Inorganic Coatings l Parylene Ultra-thin Conformal Coatings l Superfinishing l On-site Processing l Material Testing and Analysis l NADCAP, ISO 9001:2008, ISO 13485, AS9100 Rev D
www.cwst.co.uk • eurosales@cwst.com • 01635 279621
INDUSTRY NEWS
DFT INSTRUMENTS BECOMES UK DEFELSKO AUTHORISED SERVICE CENTRE DFT Instruments is proud to announced that it is now an official DeFelsko Authorised Service Centre (DASC) for the UK/Ireland, providing manufacturer-approved repairs, servicing, and recalibration for DeFelsko inspection instruments. The appointment represents a significant enhancement to the company’s service offering and delivers clear benefits to UK users of DeFelsko equipment. DeFelsko instruments are widely used across the UK coatings and corrosion protection market, supporting inspection and quality control in sectors including steel fabrication, infrastructure, oil and gas, marine, and asset maintenance. With inspection equipment playing a critical role in project compliance and sign-off, reliable performance and accurate calibration are essential. Appointment as a DeFelsko Authorised Service Centre reflects DFT Instruments’ ability to meet the manufacturer’s strict technical, procedural, and quality requirements. As a DASC, DFT Instruments is authorised to carry out certified repairs and recalibration in line with DeFelsko’s factory standards. All work is completed by technicians who have received formal training and approval from DeFelsko,
using genuine parts and calibrated reference standards. This ensures instruments are maintained to original manufacturer specifications, providing confidence in measurement accuracy and long-term reliability. For UK customers, one of the most immediate advantages is local access to authorised servicing. Previously, repairs and recalibration work required instruments to be returned overseas, resulting in extended turnaround times. By offering a UK-based authorised service, DFT Instruments a same day turn round on the majority of the range. All instruments serviced through the DASC are returned with appropriate certification and documentation, supporting quality management systems and audit requirements. This is particularly important for organisations working to recognised standards and specifications, where traceability and documented calibration are essential. The new appointment builds on DFT Instruments’ established reputation within
12
the UK market for technical expertise and customer support. In addition to supplying inspection equipment, the company has long provided practical advice and after-sales assistance to inspectors, contractors, and asset owners. Becoming a DeFelsko Authorised Service Centre enables DFT Instruments to offer a more complete lifecycle service, from initial product supply through to ongoing maintenance and compliance support. Commenting on the appointment, DFT Instruments highlighted its focus on strengthening local support for inspection professionals and reducing barriers to keeping equipment accurate and compliant. The DASC status allows the company to respond more quickly to customer needs, while ensuring all servicing work is fully aligned with DeFelsko’s global standards. Looking ahead, the appointment strengthens the availability of manufacturer-backed service capability within the UK, offering reassurance to customers who rely on DeFelsko instruments for critical inspection work. With authorised repairs and recalibration now available locally, UK users can benefit from faster turnaround, and confidence that their equipment continues to perform as intended. For the UK coatings and inspection industry, the appointment of DFT Instruments as a DeFelsko Authorised Service Centre represents a practical and welcome enhancement to after-sales support. For more information on the service available and the full range of paint test equipment from DeFelsko, please contact Mark Conlon at DFT Instruments, proud authorised UK agent for DeFelsko. Telephone: 01442 879494 Email: sales@dftinstruments.co.uk Visit:www.dftinstruments.co.uk
AT
Pull-Off Adhesion Testers Measure the adhesion of coatings to metal, wood, concrete and more Automatic Features n n n
WiFi
Impact and scratch resistant color Touch Screen display with keypad Wirelessly connect the PosiTest AT-A to your smart device using our free app Record the results as pass/fail and the nature of fracture — cohesive, adhesive and glue failures
AT-A Automatic Model
Also available AT-M Manual Model
DFT Instruments UK LTD
16A Long Drive, Meadway, Berkhamsted, Herts HP4 2PN t: 01442 879494 f: 01442 879595 www.dftinstruments.co.uk e: sales@dftinstruments.co.uk Proud supplier of DeFelsko Inspection Instruments
INDUSTRY NEWS
AVX PRO, THE NEW AIRMIX® STANDARD FOR INDUSTRIAL x® standard for industrial production lines AVX Pro, the new Airmix® standard for industrial pr PRODUCTION LINES nge ofSames automatic spray guns with the is further enhancing itsAVX range of automatic spray guns with the AV
on of the More compact, lighter, and of the AVX. More compact, lighter, an Pro,AVX. developed as a direct evolution mandsoptimized of industrial painting lines, this demands new Sames is further to enhancing range of automatic meetitsthe current of industrial painting lines, this ne spray guns with the AVX Pro, developed as a direct needsAirmix® of the wood, general industry, and spray guncompact, addresses evolution of the AVX. More lighter, andthe needs of the wood, general industry, an optimized to meet the current demands of industrial nstruction & Earthmoving). ACE (Agriculture, Construction & Earthmoving). spray gun addresses paintingapplications lines, this new Airmix ®
needs of the wood, general industry, and ACE mix® the heritage applications (Agriculture,driven Construction & Earthmoving). An evolution by the Airmix® heritage
ld feedback and the historical expertise of An evolution driven Optimizedfield feedback and the historical expertise o Developed basedbyon extensive ® since 1975, the AVX Pro mix® technology the Airmix heritage repeatability Sames Kremlin, inventor of Airmix® technology since 1975, the AVX Pr Developed based on extensive field and maintenance in atomization and air flow management. feedback and the historical expertise improvements in atomization and air flow managemen integrates targeted for industrial of Sames Kremlin, inventor of Airmix tion attechnology reduced air pressure, lowering air environments since 1975, the AVX Pro Finer atomization enables operation at reduced airdesign pressure, lowering a The gun’s has been engineered integrates targeted improvements in The AVX Pro stands out with a patented a consistent finish quality. These enhancements significantly increase transfer atomization and air flow management. to simplify maintenance, with a reduced air cap indexing system, ensuring precise finish quality. These enhanc consumption while maintaining a consistent number of parts and fast, intuitive serviceFiner life, without production rates. atomization enables compromising operation and repeatable repositioning after each replacement— even in demanding at reduced air pressure, lowering air efficiency and extend equipment service life, compromising produ intervention. This innovation reduces the without industrial environments. ®
consumption while maintaining maintenance for industrialriskenvironments of human error, improves process a consistent finish quality. These repeatability, and increases system Optimized repeatability and maintenance industrial Fullfor compatibility withenvironm enhancements significantly increase
productivity by minimizing line downtime tentedtransfer air efficiency cap indexing system, ensuring precise and existing repeatable repositioning and extend equipment installations related to cleaning and maintenance service life, without compromising The AVXafter Pro each stands outoperations. with aThis patented air cap indexing system, ensurin intervention. innovation reduces the risk of human Designed for immediate integration, production rates. the AVX Pro retains the core after intervention. error, improves process repeatability, fundamentals and each increases system Th of the previous generation: identical TCP, compatibility with error, improves process productivity by minimizing line downtime related to cleaning and existing Airmix nozzles, and easy base interchangeability. This backward productivity by minimizing maintenance operations. compatibility allows users to upgrade maintenance operations. their installations without major The gun’s design has been engineered to simplify maintenance, ®
modifications, while protecting existing investments.
gun’sreplacement— design has bee with a reduced number of parts and fast,The intuitive a reduced even in demanding industrial environments. Awith compact design number of serving productivity even in demanding industr Full compatibility with existing installations With a weight reduction of approximately 30% compared to the AVX, the AVX Pro reduces mechanical stress on equipment and simplifies integration on multi-gun lines. This compactness helps improve line availability and process stability, particularly at high production speeds.
FullPro compatibility with Designed for immediate integration, the AVX retains the core fundamentals of the previous generation: TCP, in Designedidentical for immediate ® nozzles, and easy base interchangeability. This backward compatibilityof allows fundamentals the p s without major modifications, while protecting existing investments. compatibility with existing Airmix® nozzles, and easy base interchangeabi
users to upgrade their installations without major modifications, while pro 14 oductivity
Specialists in Material Handling Solutions Product Overview Manual Monorail Systems Unit loads up to 3000kg
Monorail Chain Conveyors Unit loads up to 300kg
Power & Free Conveyors Unit loads up to 7000kg
Floor Conveyors Unit loads up to 500kg
Stewart Gill Conveyors Ltd have been supplying overhead conveyors into all sectors of industry for over 70 years. As a long time member of the Railtechniek van Herwijnen BV Group based in the Netherlands, Stewart Gill Conveyors can offer a comprehensive range of overhead conveyor products which are capable of handling unit loads up to 7000kg. Stewart Gill Conveyors Ltd offer complete manufacture, installation and commissioning, coupled with fully documented instruction, operation and maintenance manuals. We do: In-House 3D CAD engineering In-House manufactoring in the UK and EU In-House design of PLC/PC control systems Industry 4.0 Worldwide installation and commissioning Remote support, service & inspection
Part of the
Stewart Gill Conveyors Ltd Unit 3&4 Brook Business Park Brookhampton Lane Kineton, Warwickshire CV35 0JA, United Kingdom Tel: +44 (0)1926 641424 info@stewart-gill.co.uk www.stewart-gill.co.uk
n multi-gun lines. This compactness helps improve line availability and INDUSTRY NEWS duction speeds.
from the design stage A responsible
es’ CSR approach, approach integrated ng paint, air, from and the design stage , andThe AVX promoting Pro is fully aligned with Sames’ CSR approach, has featuring alsoa designbeen focused on reducing paint, air, erformance while and solvent consumption, limiting waste, and promoting component repairability. Packaging has also been optimized, supporting industrial performance while controlling environmental impact.
automatic spraying tivity, reduce line hing quality—while AVX Pro: the new Airmix standard llations. ®
With the AVX Pro, Sames delivers an automatic spraying solution designed to improve productivity, reduce
line downtime, and ensure consistent
More information at: www.sames.com
finishing quality—while seamlessly
or contact your local authorised
integrating into existing installations.
Sames Kremlin Distributor
om Distributor
Celebrating 40 years in business This year, marks five decades as an independent powder coating specialist. We are proud to have one of the largest ranges of stock powder coatings in the UK, available for next day delivery. We have thousands of satisfied customers across diverse markets including construction, agriculture, leisure and retail as well as renowned architects and design houses.
RETAIL
AGRICULTURE
ARCHITECTURE
LEISURE
CONSTRUCTION
Talk to us about our expert colour matching services that offer first class industry lead-times. Challenge us to find you a solution!
01827 55777
www.thermaset.co.uk
2040 Trade Mag Advert_TradeAd [V6 REPRO].indd 2
enquiries@thermaset.co.uk
15/05/2024 17:34
INDUSTRY NEWS
WITHAM GROUP ANNOUNCES TWO NEW BOARD APPOINTMENTS TO DRIVE STRATEGIC GROWTH ensure Witham Group continues to blend
Leading UK lubricant manufacturer, The Witham Group, is pleased to announce the appointment of two new members to its Board of Directors to help shape the organisation’s future strategic direction.
market-leading lubricants. Ian Wright joins the board as Operations Director. Ian’s impressive 17-year tenure with the Witham Group began in the Lincoln factory before he transitioned into
Graham Dawson and Ian Wright bring a
information systems of the business.
wealth of industry expertise and internal
Known for his analytical mindset, process
insight to the board, having both served
optimisation skills, and deep commitment
as Associate Directors for the past two
to customers and suppliers, he has
years.
become a vital asset to the company. In
Graham Dawson has been appointed as
his new role, Graham and his team will
Commercial & Technical Director. Since
expand their remit to lead the technical
joining the Witham Group seven years
aspects of the business alongside
ago as Commercial Manager, Graham has
commercial operations. This includes
overseen the day-to-day finance,
leading development in the latest
Lubricants Association (UKLA). In his new
administration, and management
technologies and product ranges to
capacity, Ian will remain an advocate for
the administrative Operations Team. Over nearly two decades, he has managed key accounts and established himself as a trusted, “go-to” partner for many of the company’s long-standing customers. His exceptional contributions early in his career earned him the prestigious nationwide Young Employee of the Year award from the United Kingdom
customer service, high manufacturing standards, and operational team development, while heavily focusing on driving the company’s key environmental objectives. Nigel R. Bottom, Managing Director of Witham Group, commented: “We are delighted to welcome Graham and Ian to the main board. Together, they bring a combined 24 years of deep operational experience within the Witham Group. These appointments significantly strengthen our leadership team and demonstrate our commitment to rewarding internal talent, while ensuring we are robustly positioned to navigate the future and deliver the highest standards of product innovation and service for our customers.” Graham Dawson, Nigel R Bottom, and Ian Wright.
18
Visit: https://www.withamgroup.co.uk/
Scan Spray
&
Dynamic Contour Detection Programming-free coating of any shape! The second generation of Dynamic Contour Detection detects the object contour fully automatic and positions the guns individually even for thin objects and at high conveyor speeds. Due to the programming-free adaption of all relevant line settings the application range is significantly extended.
Gema Europe Srl – UK Branch Tel: 0044 1202 763 942 Email: uk.sales@gema.eu.com
gemapowdercoating.com
INDUSTRY NEWS
A LEADING PLATFORM TO EXHIBIT SFCHINA2026 will be held from November 11 to 13, 2026 at Area A of the China Import and Export Fair Complex in Guangzhou, P.R. China. Since its inception in 1983, SFCHINA has grown into a leading surface finishing platform for technology exchange and business development across Asia and beyond. To better reflect its expanding scope, this year’s exhibition will introduce 2 redefined exhibit zones: “Electroplating & Finishing Technology” (Zone 1), and “Coating Equipment, Engineering & Services | Special Function Coating Products” (Zone 2), enabling exhibitors to present targeted solutions while helping visitors to navigate the exhibition more efficiently.
Exhibit to Capture Growth Momentum The global surface finishing market was valued at US$3.5 billion in 2025 and is projected to reach US$5.1 billion by 2031, growing at a CAGR of about 7.5%. Asia Pacific currently accounts for 35 – 40% of global revenues, with China emerging as the fastest-growing market in the region. This growth is driven by increasing demand from key end-use sectors such as applications in automotive (particularly new energy vehicles), aerospace, electronics and sustainable construction.
20
Exhibiting at SFCHINA places businesses at the centre of this strategic and rapidly expanding region.
Seize Opportunities in the Greater Bay Area (GBA) Guangzhou sits at the heart of the Guangdong-Hong Kong-Macao Greater Bay Area, one of the world’s most dynamic economic regions. In 2025, the GBA’s GDP surpassed RMB¥15 trillion, which ranks it among the world’s top 10 economies. Growth is expected to
continue through 2026, driven primarily by advanced manufacturing, new energy vehicles, semiconductors, green building materials and smart infrastructure. SFCHINA offers exhibitors direct access to this thriving hub, enabling them to leverage cross-border trade opportunities and broaden their customer base.
Align with National Priorities China’s 15th Five-Year Plan, beginning in 2026, emphasizes sustainability, smart manufacturing and advanced materials as
INDUSTRY NEWS
key drivers of industrial transformation. Exhibiting at SFCHINA2026 enables companies to showcase innovations that align with these priorities, from eco friendly processes and high performance coatings to intelligent production technologies and advanced finishing solutions. By presenting solutions that address both policy goals and industry needs, exhibitors can strengthen their positioning in China’s surface finishing market and forge stronger connections with downstream sectors undergoing modernization.
A Proven Leading Platform For over 40 years, SFCHINA has evolved into a leading platform for exhibitors to present new technologies, strengthen brand visibility and connect with decision-makers face-to-face. The 2025 Shanghai edition welcomed 8,510 visitors from 40 countries / regions, representing a 16.2% increase compared with 2024,
and hosted 303 exhibitors from 17 countries / regions, an 8.6% increase. These figures highlight the exhibition’s role to create important opportunities for exhibitors to connect, grow and collectively contribute to the industry’s development.
To learn more about SFCHINA2026, please visit www.sfchina.net for more details, and follow us on Facebook, X, LinkedIn and YouTube to stay updated. Scan the QR Code to apply to exhibit.
ay
pr
rs
ai | ss
rle
ai m pu
Built with 65 years of design and engineering excellence.
ps
m
pu
Industrial Spray Equipment
ps
Designed for precision, engineered for performance, Elcometer spray equipment is built to work harder, last longer and perform better.
| ss
ra
ai ed
ist ss
rle
ai m pu ps s|
ay
s
re
e
u ss
pr Surface World - Ella.indd 3
t po
|
r sp
n gu
l
r fi
ai
n
io
t tra
SPRAY IT elcometer.com
12/05/2025 07:45:22
AEROSPACE & MARINE
CORROSION PREVENTION IN AEROSPACE AND MARINE ELECTRICAL SYSTEMS Electrical corrosion costs both private and public sectors hundreds of billions a year in repaired or replaced electrical, electronic and avionic components, but there are cost-effective, proven ways to prevent it that should sit at the heart of any preventative maintenance programme. Electronic and electrical equipment used in adverse environments is regularly exposed to corrosive gases, causing rapid deterioration of connectors, switches and control components. The risk is particularly acute wherever close-tolerance or dissimilarmetal components are in contact, which is common in plated, anodised and galvanised assemblies where localised galvanic corrosion can accelerate failure long after finishing is complete. Salt spray and changes in temperature and humidity present a further threat to bearings, actuators, electrical connections, high-voltage mating, switches and contactors. The failure of any of these components presents potential dangers to equipment and passengers. Preventing corrosion involves a combination of preventive measures. An essential first step is applying a protective coating, such as SuperCORR
24
A, which helps prevent galvanic, fretting, dissimilar-metal, intergranular, hydrogen sulphide, salt and chloride corrosion in electrical and electronic equipment, and ensures longevity and reliability wherever exposure is a concern. Other measures include selecting resistant materials such as stainless steel or nickel alloys over carbon steel; sealing equipment in corrosion-resistant, ventilated enclosures; regular monitoring with early-warning gas detection; considering equipment design and location to reduce exposure; and having trained personnel and an emergency response plan in place should exposure occur.
AEROSPACE & MARINE
SuperCORR A specialist barrier
ARMY: 1-1500-344-23.
film corrosion protection
NAVY NAVAIR 16-1-540.
SuperCORR A is a proprietary formulation supplied by
AIRFORCE: T.O.1-1-689,691,700, 35-1-3.
EnviroTech Europe, based on approved synthetic materials, with long-lasting anti-corrosion inhibitors. It provides a superior
BOEING Part No. 12-371.
lubrication coefficient alongside protection against moisture,
Extensive testing has shown that SuperCORR A significantly
wear, general and fretting corrosion, static electricity, corona
reduces “no fault found” incidents: intermittent failures caused
and other electro-migration problems. The non-flammable film
by corrosion at contact points that clear once a component is
is just 7 microns (0.007mm) thick, will not harden or crack,
removed and re-seated. Its dual function as corrosion inhibitor
and is formulated without sulphates, chlorides, petroleum-based
and dry lubricant makes it equally effective on close-tolerance
material or halogens, meeting the EU RoHS directive.
and dissimilar-metal components, protecting contact surfaces
SuperCORR A forms an airtight seal preventing damage to
without interfering with tight mechanical tolerances.
electronics and other surfaces caused by exposure to fresh
SuperCORR A has been used by the U. S. Air Force to protect
and saltwater moisture and corrosive gases including Sulphur
the intricate workings of the F-16 Fighter Jet and by the
dioxide (SO2), Nitrogen dioxide (NO2), Hydrogen Sulphide (H2S),
U.S. Navy on the P 3 Orion electronic surveillance aircraft.
Ammonia (NH3), and Chlorine (CL12) based gases, and the
Commercial aviation aircraft manufacturers also benefit from its
thermal decomposition byproduct of HFC-227ea used in fire
use on electrical and close mechanical applications, especially
suppression systems, Hydrogen Fluoride (HF). It is the ultimate
on routes involving salt fog exposure or flights over open sea
corrosion protection formulation for aircraft, marine and a wide range of other industrial sectors. Packaged in aerosol cans, it’s easily applied by engineering crews even in difficult-to-reach locations.
HISTORY SuperCORR A was originally developed for the U.S. Air Force to comply with military specifications and to prevent electrical and electronic components from systems failures caused by corrosion. It became the industry standard for avionic corrosion protection within MROs (maintenance, repair and operations) and OEMs (overhaul and original equipment manufacturers). It’s unique ability to displace water and provide a performance enhancing level of corrosion protection has led to it being used in many other applications and industries worldwide.
CASE STUDIES
INDUSTRY APPROVALS
BELOW - Corroded PCB in aircraft control system.
Approved in US Tri-service corrosion manuals and military,
Corrosion of electrical components is very prevalent problem
civilian and aircraft manufacturers, railway and transport
and preventing moisture from coming in to contact with the
operators worldwide.
electrical components is essential.
MIL-DTL-87177B (revised MIL-L-87177A) Type I, Grade B “Avionics Cleaning and Corrosion Prevention/Control”. Exceeds Mil C 81309 Corrosion Prevention Compounds. Approved in US Tri-Service Corrosion Manuals.
26
A leading international computer manufacturer tested SuperCORR A for evaporative weight loss, a key indicator of corrosion-inhibitor and lubricant effectiveness, it recorded a weight loss of just 40% after 1,000 hours of exposure at 80°C (30% after 160 hours), the lowest of all materials tested.
FINISHING SYSTEMS
Global Leadership in Automated Finishing Systems Comprehensive Lifecycle Management KOCH manages finishing systems from concept to long-term support, ensuring seamless integration and reduced project risks.
Wide Range of Coating Technologies KOCH offers turnkey solutions for liquid paint, powder coating, electrocoating, anodizing, plating, and porcelain enamel.
Focus on Sustainability and Efficiency Systems are built with energy-efficient technologies and eco-friendly features like wastewater and emissions control.
Global Reach with Local Expertise KOCH operates globally with local presence in the US, Mexico, and Europe for close customer collaboration.
Contact: 044 (0) 1543 444001 sales@kochllc.com www.kochllc.com
AEROSPACE & MARINE
BELOW - Mild steel panels exposed to sea spray for six months showed severe rust on both an untreated section and one
Displaces both fresh and saltwater moisture.
treated with SuperCORR A remained visibly protected
Prevents deterioration and contamination on all surfaces of electronic and electrical equipment and mechanical close tolerance moving components.
throughout.
Does not attract contaminants, non-reactive to most plastics.
protected with a conventional oil-based CPC, while the section
Eliminates premature failure of components created by moisture, general or fretting corrosion. Reliability increased, maintenance intervals increased, costs reduced, manufacturers save costly warranty service calls or product re-call. Inert compound that neither reduces nor increases electrical conductivity and will not increase or decrease contact resistance. Eliminates surface static electricity, corona and other electro migration problems in electronic circuit boards and connectors. Will not freeze or harden, retains properties even in high-altitude applications. Extremely resistant to air-drying and self-healing. A: Oil based CPC
Decomposition temperature of 550°F.
B: Untreated section C: Treated with SuperCORR A demonstrating its superior performance. SuperCORR A keeps unpainted mild steel from rusting on exterior surfaces directly exposed to sea water environments for at least 6 months, protecting electrical connectors, switches, chains and drive shafts from corrosion while maintaining
FURTHER INFORMATION
lubrication on moving surfaces.
Please visit our website https://www.envirotech-europe.com/ supercorr-a for information about other uses and applications for SuperCORR A.
CONCLUSION For aerospace and marine operators, SuperCORR A offers a proven way to prevent galvanic, fretting and salt-induced corrosion from destroying electronics and electrical components. It was specifically designed to lubricate and protect electrical fittings and connectors; electrical and avionic harness assemblies and connectors; electrical and electronic switches; close-tolerance and dissimilar-metal components; and lighting connectors and sockets, keeping critical systems reliable in the harshest operating environments. The use of SuperCORR A brings financial savings through reduced maintenance and replacement costs and, more importantly, greater safety. Prevention is always simpler and less costly than repairing or replacing failed equipment.
FEATURES AND BENEFITS Extremely long-lasting, specially formulated and proprietary anti-corrosive inhibitor.
28
For more advice, please telephone us on +44 (0) 20 8942 9177 or use our website contact form. Manufactured in the United Kingdom and available on short delivery times through our dedicated team of distributors worldwide.
PROTECT YOUR VALUABLE SURFACES.
Solutions for recycling
SOLVENTS Save Money | Recycle Any Solvent High Yield | Low Waste
• Units available for any quantity and application • Safe and easy to use
UY B OR LEASE
• Recycled solvent as good as new • Atex certified for flammable solvents • The number one choice with over 38,000 units worldwide
Automated protection tape application for all kind of profiles or flats in different materials. Single-sided, double-sided, four-sided, flat or round surfaces – our machines match all your requirements.
ASK FOR
A FREE
QUOTE
SOLVENT
SYSTEMS
For more information visit:
www.solutex.co.uk info@solutex.co.uk | 01691 622 225
We're excited to introduce a recent addition to our portfolio: our new
Cabinet Parts Washer.
SWISS MADE
RECYCLING
T +41 44 926 44 88 sales@muller.ch www.muller.ch
NEW PRODUCT ALERT!!
Their fully Welded stainless Steel construction and Hygienic Design significantly reduces and minimises the need for extensive and time consuming cleaning operations. The units are mobile, can be fitted with extraction fan or condensate unit (as shown) and feature a self-contained water storage tank and filter tank, which effectively removes gross debris and particulates before draining. If you have similar requirements or are interested in exploring our range of equipment for the Food, Pharmaceutical, and Engineering sectors, please don't hesitate to reach out to us.
Email us: washers@unitech.uk.com or Call us: 01543 224608
ELECTROPLATING, ANODISING & GALVANIZING
MEDIUM-TEMPERATURE SEALING PROMISES ENERGY SAVINGS are potentiated Due to rising energy prices, energy-rich processes such as the anodising process continue to be in strong focus. With its medium-temperature sealing, Chemetall a manufacturer of specialty chemical products supplies an additive that can achieve considerable energy savings in the compression process. Electrolytic anodising of aluminium is one of the most energy-intensive finishing techniques in surface treatment due to its high power and energy requirements. Especially in the last treatment step, bath temperatures of up to 98°C are required during hot sealing. With the Gardo Seal 1999, Chemetall supplies a Qualanod-approved mediumtemperature sealing system that enables energy savings of up to 30%.
Energy savings that
By using 0.3% Gardo Seal 1999, a classic hot sealing bath can be converted to a medium temperature sealing. For this purpose, the operating temperature can be reduced by approx. 10°C from 98 to 88°C. The sealing times remain at a maximum of 3 min/µm. Gardo Seal 1999 ensures both a residue-free surface and good compaction values.
the sealer at 88°C is reduced by up to 30%. In addition, the reduction in evaporation means that the entire plant structure, the transport system plus the employees are exposed to less water vapour. Thus, the use of the Gardo Seal 1999 reduces the corrosion effects on the plant technology and improves the plant management.
Increase flexibility
By lowering the temperature, there are a number of energy saving opportunities. First, of course, there is the obvious saving due to the lower heating of the bath and the reduced energy input during temperature maintenance. The achieved temperature difference of ~10°C saves 10 to 15% energy during heating up to the operating temperature of 88°C. In addition, the holding temperature of 88°C saves a further 10 to 20% energy compared with conventional hot sealing.
Not only can energy savings be achieved by using the Gardo Seal 1999, it can also increase the end users flexibility due to its high performance at high temperatures.
Another point worth mentioning, is the reduction of evaporation. Although sealing balls often minimise the greatest evaporation effects, further benefits can be achieved by lowering the temperature. For example, the internal vapour pressure and the associated evaporation rate of
Although the sealing baths in an anodising plant do not usually represent the immediate bottleneck, there are various scenarios that certainly support an increase in throughput. Chemetall works with the end user to determine the highest possible potential for optimisation. This can be savings of complete anodising baths, additions of anodising baths to increase throughput or shortening of anodising times.
For example, at an application temperature of 98°C, Gardo Seal 1999 can achieve reduced compaction times of 2 min/µm and beyond. This means a time saving of up to 33% compared to a classic hot sealing, while at the same time achieving optimum compaction values.
Further potential The full potential of saving energy or increasing throughput is demonstrated by the combination of Gardo Seal 1999 with the anodising additive Gardobond Additive H 7526. This product combination enables customers to run up to 30% higher throughputs on an anodising line while maintaining the same quality. The flexibility of the system allows customers to decide for themselves whether they want to focus on energy savings or on increasing throughput. Visit: www.chemetall.com
30
Thru-process Monitoring Solutions for Paint & Powder Coating Ovens Temperature Profiling Systems
Comprehensive Range • Data Logger and Thermal Barrier choice (6 to 20 Thermocouples) • Extensive Thermocouple range • Real Time RF Telemetry options • ATEX approved options • Full UK service and calibration support
Oven Profile and TUS software
Software Packages to Suit • Thermal View or enhanced Thermal View Finishing software - Match Analysis Tools to suit. • CQI-12 Temperature Uniformity Survey solution options
Optic Video Profiling System
Innovative Video Capture Thru the operating oven
• Detect paint runs, chips and defects • Spot transport problems • Identify oven damage • Locate dust and inclusion risk areas
Visit us for more information: PhoenixTM Ltd UK sales@phoenixtm.com
www.phoenixtm.com
PhoenixTM LLC USA info@phoenixtm.com
PhoenixTM GmbH Germany info@phoenixtm.de
Monitor, Control, Improve & Certify....Your Coating Process
!
ts n u o c e ic o h c & nce ...where experie
ELECTROPLATING, ANODISING & GALVANIZING
POLYPLAS ENGINEERING LTD HAVE BEEN SERVING THE FINISHING AND PLATING INDUSTRY FOR 40 YEARS The finishing and plating industry remains the company’s main customer base. We can support your needs from single tanks and bespoke CNC machined components to full plating lines and turn key solutions, including integrated fume extraction systems and pipework and bunding with GRP gridding walkways etc. We offer a full installation, repair and maintenance service.
32
Our core business, which we excel at, is tank design and fabrication. Using RITA 5.1 Software to design tanks, ensuring the design, manufacture and tank integrity meets BS EN 12573, you can be confident your requirements are manufactured to a high standard. The quality of our fabrications is of paramount importance and our Plastic Fabricators are qualified and certified to BS EN 13067 in all disciplines of Plastic Welding certified by CSWIP accreditation, delivered by The Welding Institute, one of a very few companies in the UK to have invested in this.
PolyPlas Engineering also manufacture, in-house, complimenting steel fabrications, such as access ladders, walkways, work platforms etc We also provide a Tank Inspection Service which has proven very useful for many new and existing customers, often satisfying HSE requirements for storage of hazardous chemicals. Plastic tanks may have been installed previously, which do not meet BSEN standards, or are not frequently inspected, exposing operators to increased risk of accidents, increased costs and potential prosecution. PolyPlas Engineering has extensive
Protection upgraded
Trivalent Decorative Chromium Plating SurTec 883 XT - Trivalent Decorative Chromium Process Identical colour values as chromium(VI) surfaces Integration into existing lines possible Excellent layer thickness distribution between 0.2 and 0.4 μm
SurTec 851 - Exclusive Satin Nickel Finish Semigloss & non-reflecting nickel coatings with extreme uniform finish Long bath lifetime due to using a continous system Broad range of satin effects to match automotive OEM requirements
SurTec 866 - Bright Acid Copper Process For extremely bright copper deposits with excellent levelling Well suited for parts with deep recesses or complicate shapes Very efficient additive system with low maintenance cost
SurTec Group UK Office Nigel Wicks
+44 7841 527552 Nigel.Wicks@SurTec.com
ELECTROPLATING, ANODISING & GALVANIZING
experience in helping industry mitigate
Three automated sheet butt welding
these risks by providing an inspection
machines, welding plastic sheet up
service and reporting of potential
to 3000mm x 50mm thick solid
risk issues.
plastic sheet
Within the industry we have an
CNC routing of sheet materials
excellent reputation for competitive
3000mm x 2000mm (3 machines)
pricing without compromising on quality. Please visit the gallery page on our
Site work, maintenance and repairs In house metal fabrication & welding
website www.plasticfabricationservices.
PolyPlas Engineering Ltd is part of
co.uk shows many of the quality
The Poly Group, which offers a full
fabrications PolyPlas Engineering have
stack plastic manufacturing service,
manufactured, and shows the diverse
including our including rotational
nature of work and manufacturing
moulding and vacuum forming
capabilities.
business. We mould products as large as 4.5m x 2m and have one
Amongst our many services we offer
of the longest vacuum forming
the following specific manufacturing
machines in the UK at 4.6m x 1.6m.
capabilities:-
We provide products design and
Tank & vessels designed & manufactured to BS EN 12573 using RITA 5.1 design software Plastic welding in all disciplines to BS EN 13067. Our time served skilled fabricators are qualified and certified
tolling specification service, product assembly and finishing and electrical testing of products. Please contact us to discuss any requirements you have and how we can support you.
by CSWIP accreditation.
Telephone Number – 0114 2481973
Computer drawing packages
Email Address –
& design capability
info@plasticfabricationservices.co.uk
Butt & socket fusion of plastic
Website Address –
pipe & fittings
www.plasticfabricationservices.co.uk
34
PHOS-PREP
®
Pre-Treatment Solutions Group Ltd supply unique che chemistries for an array of metal processes. Our Phos-Prep® range of chemicals are chrome free, eco-friendly and cost effective all while maintaining quality and performance. With over 50 years experience within the industry we pride ourselves on finding the right solution for your metal treatment. Whether that be degreasing, etching, phosphating, paint stripping and more!
TESTIMONIALS “We have been a customer of PTS for over 20 years and during our time we have relocated our business, changed our pretreatment process with the full support and expert advice to implement changes from the PTS team. A great company who always go the extra mile to support their customers.” P.Allen, West Midlands. “We have been fortunate to have partnered with PTS for over ten years now. They are consummate professionals and always exceed expectations in terms of delivery of service, knowledge and customer care.” E.Smith, Hampshire. “We have had the great pleasure in working with PTS for over 5 years. No matter how big or small our queries are, PTS always come up trumps and in rapid time. The team are always willing to visit our site to help out with any issues we have or just for a general catch up with our staff. We have a very good relationship with the whole team at PTS and long may this continue.” R.Glasbey, West Yorkshire.
02475 090 133 Sales@PTSGroupUK.com www.pretreatmentsolutionsltd.com
ELECTROPLATING, ANODISING & GALVANIZING
PERIODIC PULSE RECTIFIERS: ENABLING STABLE TRIVALENT CHROMIUM PLATING The transition from hexavalent to trivalent chromium plating continues to reshape the metal finishing industry. While trivalent systems offer clear benefits in terms of environmental impact and operator safety, they also introduce tighter process windows and higher sensitivity to electrical parameters. As a result, the rectifier is no longer just a power supply—it has become a critical process tool. Periodic pulse rectifier (PPR) technology plays a key role in meeting these new demands. Trivalent chromium deposition requires precise control of current density, waveform, and timing to achieve consistent thickness, colour, and surface quality. Unlike conventional DC operation, periodic pulse current allows the electrochemical reaction to be actively managed. Pulse on-times drive deposition, while off-times allow ion diffusion and surface relaxation, reducing burning and improving coverage on complex geometries. One of the key requirements for pulse rectifiers in trivalent chromium plating is accurate and stable waveform control. Frequency, duty cycle, and current amplitude must be adjustable with high resolution and repeatability. Even small deviations can result in color shifts, dull deposits. Fast rise and fall times are essential to ensure that the defined pulse shape is maintained regardless of load changes or rack movement. Low ripple performance is equally important. Trivalent chromium baths are
36
particularly sensitive to ripple, especially at the lower current densities used in decorative applications. Excess ripple can lead to visible surface defects and uneven appearance. A modern pulse rectifier must therefore combine dynamic pulse modulation with extremely low residual ripple under all operating conditions. Periodic pulse reverse (PPR) waveforms add another layer of process control. By introducing a controlled reverse pulse, desorption occurs at the cathode surface, helping to balance low and high current density areas. This improves uniformity, enhances throwing power, and supports more consistent plating on parts with challenging shapes. In decorative trivalent chromium plating, pulse and reversepulse techniques can also improve appearance, producing brighter, bluer, and more uniform finishes. While pulse plating is gaining momentum in general metal finishing today, it is a well-established and proven technology. For over 30 years, KraftPowercon has supplied PPR rectifiers globally for demanding PCB applications where precision and repeatability are critical. This long experience has shaped a deep understanding of pulse behaviour, and reflected in the ModuPulse rectifier platform. Designed for advanced plating applications, ModuPulse delivers highresolution pulse and reverse-pulse
control, ultra-low ripple, and robust performance in continuous industrial operation. Its modular architecture allows easy scaling and adaptation to different bath chemistries and process recipes, while modern communication interfaces support seamless integration into automated plating lines. As trivalent chromium continues to replace traditional technologies, periodic pulse rectifiers are becoming essential for achieving consistent quality and efficient operation. With ModuPulse, KraftPowercon combines decades of PPR experience with a future-ready platform—helping metal finishers fully realise the potential of trivalent chromium plating. Contact us (Bjorn.Ulfvenskold@ kraftpowercon.com; +46 31 979718) to discuss how ModuPulse can strengthen your plating performance.
Learn more about KraftPowercon’s PPR rectifiers ModuPulse:
We solve our customers filtration, chemical transfer and treatment needs.
Contact us
SIEBEC UK Ltd, Stafford +44 (0) 1785 227700 sales@siebec.co.uk www.siebec.co.uk
PUMPS & FILTERS
FILTER MEDIA
SPECIAL SYSTEMS
L SERIES | Medium flow rate filter P SERIES | Ultra-high flow rate filter A SERIES | Mechanical seals pump M SERIES | Magnetic drive pump T SERIES | Vertical pump [...]
L-TECH | Pleated cartridge BAGTECH | Filtration bag QUALITHERM | Extruded cartridge QUALIBOB | Wound cartridge ANODTECH | Anode bag [...]
ACIDPURE | Acid recycling EASYPURE | Fluid recycling IONPURE | Ionic filtration ACIDVAC | Acid draining vacuum EDUCTORS | Bath agitation [...]
NE W
Oven Temperature Logger Measures and records oven temperature profiles
6 K-type thermocouple ports
High temperature stainless steel barrier box for long run times
Download, view, and analyze data using PosiSoft Desktop Software or export to .CSV
Prices starting at: Oven Temperature Logger..........£1895 Temperature Probes............£100
Wide variety of spring clamp and magnetic temperature probes available
Customizable PDF Reports
16A Long Drive, Meadway, Berkhamsted, Herts HP4 2PN t: 01442 879494 www.dftinstruments.co.uk e: sales@dftinstruments.co.uk
ELECTROPLATING, ANODISING & GALVANIZING
THE BEST KEPT SECRET IN THE INDUSTRY IS JUST A LOAD OF BALLS! “Euro-Matic’s croffles solution solves so many manufacturing issues, why doesn’t everyone know about it?” Let’s face it, it isn’t a new thing, a croffle, in fact Euro-Matic have been producing them since 1965 and have been selling them globally, but its surprising how many people don’t know about them or what a simple, cost effective solution they are for the manufacturing environment. For any factories or production plants with chemical processes or heat or cooling tanks there will inevitably a number of knock on effects, such as maintaining tank temperature and the costs associated with this and also the nasty smells, toxins or even just the damage evaporation can do to the work place environment in respect to decay of buildings and the workforce. But this long-standing simple solution that has been development by Euro-Matic solves these issues simply by pouring blanket of balls onto any open process tanks and creating a flexible cover. A blanket of Euro-Matic croffles reduce heating costs by up to 75%, and evaporation by 90% and they last for years. Euro-Matic balls come in a variety of plastics such as HDPE and most commonly PP dependent on the chemicals and a variety of sizes from 6mm right up to 150mm. The cool thing is that the balls move around any parts in machinery and by sitting on the top of the liquid, there is completely no maintenance. We have many satisfied repeat customers from chrome and electroplating to automotive and what is simple is that they are literally poured on to the tank with immediate benefits.
How to get some balls Balls can be ordered on line at www.euro-matic.co.uk or by calling them on 0330 311 0003 where their friendly staff will work out exactly how many you need, there is also a clever ball calculator that enables you to insert tank dimensions and it will do the maths for you, https://www.euro-matic.co.uk/ball-calculator/ Euro-Matic supply direct and or to distributors. Stock is all available next day from their Midlands distribution hub.
38
Haviland Ltd
Specialists in design & manufacture of bespoke pre-treatment systems, industrial ovens, paint or powder booths with manual and automatic conveyor systems
Conveyorised Powder Coating Systems Ovens; Conveyor, Box, and Radiant Metal Pre-treatment Systems Powder and Wet Spray Booths Oven Servicing
Contact Us
Tel: 01159 444 159 Email: haviland.ltd@outlook.com Web: haviland.ltd.uk
TESTING & MEASUREMENT
NEW: BYKO-SPECTRA LED 6 Color appears differently. We make it consistent. BYK-Gardner – a worldwide partner of the automotive, paint, and plastics industries for quality control of color, appearance, and physical properties – is introducing the new bykospectra LED 6. This light booth represents the next generation of standardized LED illumination for visual color assessment and sets new benchmarks in precision and reproducibility. As traditional incandescent and fluorescent light sources are increasingly being phased out due to their high energy consumption and hazardous material content, the byko-spectra LED 6 is based entirely on modern, sustainable LED technology. Its smart LED module simulates all CIE standard illuminants with outstanding accuracy and delivers stable, reproducible spectral power distributions that significantly outperform those of conventional fluorescent lighting systems. The byko-spectra LED 6 offers a wide range of standardized illuminants, including daylight D65 at the highest quality level (MIvis Class A) and various
40
warm-white LED illuminants, such as LED-A, LED-B1, and LED-B2, which represent typical retail lighting conditions. In addition, LED-B3 enables the realistic simulation of lighting environments commonly found in modern retail stores, characterized by a cool, fresh light appearance. Optional UV illumination can be activated for the evaluation of optical brighteners and fluorescent effects. This allows all relevant everyday lighting situations to be reliably simulated – from natural daylight and residential lighting to modern retail environments. The precise reproduction of these conditions ensures that colors and materials can be evaluated consistently under various lighting scenarios. In addition to its advanced lighting technology, the byko-spectra LED 6 features a compact yet modern design. The light booth fits easily on standard laboratory benches while still providing ample space to evaluate samples up to 64 × 48 cm (25 × 19 in). The exterior walls are robust, and the interior surfaces are finished in matte light-gray Munsell N7, providing a neutral and controlled viewing environment. A long-life diffuser ensures uniform illumination across the entire viewing area, fully meeting the
requirements of international standards such as ASTM D1729 and ISO 3668. The light booth can also be assembled quickly and without special tools, enabling fast and straightforward installation. For maximum ease of use, the bykospectra LED 6 is equipped with a large touchscreen display. Users can switch between illuminants directly, adjust light intensity, and monitor key parameters such as correlated color temperature. Fast switching between illuminants and the display of the remaining LED lifetime support efficient workflows. An automatic sequencing function allows predefined lighting conditions to run consecutively, enabling reproducible color evaluations without manual intervention. With the introduction of the byko-spectra LED 6, BYK-Gardner further strengthens its position as a technology leader in colorimetric and visual quality control. The combination of advanced LED technology, a compact and durable design, and intuitive operation establishes a new standard for reliable, precise, and standards-compliant visual color assessment in industrial and laboratory environments. More information is available from BYK-Gardner GmbH at www.byk-instruments.com
Measure the visible and beyond.
Find out which is the right color meter for you Precise Color & Gloss Anywhere The color2go spectrophotometer combines precise color and 60° gloss measurement in a compact design. A large touchscreen ensures intuitive, smartphone-like operation. Digital standards enable consistent results across the supply chain. The device warns users if fluorescence is detected and includes the powerful yet easy-to-use smart-chart data analysis software.
Affordable Start to Color Control For tight budgets, the color2check offers an affordable entry into color control. Compact, lightweight, and robust, it ensures easy handling and reliable results. Its intuitive touchscreen and protective garage enable safe use and storage. The proven BYK LED ensures stable performance, with no calibration required for up to 3 months.
www.byk-instruments.com
PUMPS & FILTRATION
EcoPump GW iD – reliable coating application quality for industrial applications
NEW GEAR-TYPE METERING PUMP FOR PRECISE PAINT DOSING Dürr is launching an optimized gear metering pump designed specifically for use with common 1K and 2K coating materials in industrial coating processes. The new pump is designed with a focus on durability, ease of use, and cost efficiency. The new EcoPump GW iD series is suitable for a wide range of industrial coating applications that require precise volumetric delivery of consistent amounts of coating. With flow rates ranging from 9 to 900 ml/min, the pump can be adapted to different applications as required. In addition, the pump is compatible with
Dürr’s ready2integrate concept. This concept ensures that the control system, metering technology, and applicator are optimally coordinated and delivered as a preconfigured solution. Customers benefit from quick installation, high process reliability, and a solution tailored to their specific requirements.
Figure 1: The EcoPump GW iD is designed for industrial painting processes.
Reliable paint finish quality and high process reliability To meet the high demands of industrial coating processes, all models come standard with an Amorphous DiamondLike Carbon (ADLC) coating. This coating ensures high durability and helps maintain surface quality over the long term. For added operational reliability, the EcoPump GW iD is optionally available with a bypass valve. In addition to its pressure-relief function, the valve opens automatically in the event of overpressure, thereby reliably protecting the downstream application equipment from potential operating errors and process disruptions. Furthermore, the flushable models feature a patented shaft bearing. This significantly extends the pump’s service life, resulting in lower maintenance and repair costs while enhancing operational reliability.
Flexible integration into compact dosing systems The EcoPump GW iD is part of the Fluid Board2, which combines all the components required for high-precision paint metering within a compact space. This allows the system to be easily and efficiently integrated into painting processes. For existing applications, the pump can also be retrofitted onto the Fluid Board1, offering additional flexibility during upgrades. Furthermore, the new EcoPump GW iD is compatible with existing systems and can be retrofitted as a standalone component at any time.
42
HMA 2A
TX
FDB
High efficiency
Choice of operating fuels
Customised design to suit each install
Ideal for variable plant conditions
Reduced NO₂/CO Emissions
Proven in a wide range of applications
Larger heat input available on request
Air replacement or “Make-Up”
Choice of burner heat inputs up to 1150 kW
APL technology -modulating gas and air
Up to 30:1 turndown Up to 205 kW per foot
FDGA APL technology - modulating gas and air Ideal for variable plant conditions Heat input range up to 1,550 kW Choice of operating fuels
BESPOKE DESIGN
Our gas burner systems offer users reliable, high efficiency, process heating solutions. From design, manufacturing and supply to installation, commissioning and ongoing support, we fulfill process liquid, oven and air heating needs for both new-build and conversion projects.
FULL RANGE OF INTERNATIONAL ACCREDITATIONS
FDC Heat input range up to 1,550 kW Choice of operating fuels Packaged burner design Up to 40:1 turndown
BURNERCARE SERVICE
Lanemark Combustion Engineering Limited Lanemark House, Whitacre Road, Nuneaton Warwickshire CV11 6BW United Kingdom
BENEFIT FROM GLOBAL SOLUTIONS DELIVERED WITH THE CONFIDENCE OF LOCAL SUPPORT
When it comes to heavy equipment, there’s no room for error. From demanding durability requirements to exacting color and finish criteria, the toughest of applications require the most formidable of solutions.
Contact: gi.emeai.marketing@sherwin.com Visit: www.sherwin-williams.eu
info@lanemark.com +44 (0) 24 7635 2000
PUMPS & FILTRATION
About Dürr Dürr Systems AG is part of the Dürr Group and operates globally in the automotive industry and other markets, specializing in painting technology, final assembly, dispensing technology, and consulting. As a market leader, Dürr designs and implements turnkey systems and manufactures high-quality machines and robotic technology as well as production lines for battery electrodes. The company has proven expertise in digital and sustainable solutions. As of 2025, Dürr Systems AG employs around 6,700 people. The Dürr Group is one of the world’s leading mechanical and plant engineering firms with particular expertise in the technology fields of automation, digitalization, and energy efficiency. Its products, systems, and services enable highly efficient and sustainable manufacturing processes – mainly in the automotive industry, for producers of furniture and timber houses, as well as in the assembly of medical and electrical
products and in battery production. The Dürr Group generated sales of just under €4.2 billion in 2025 and currently has around 17,500 employees and 123 business locations in 32 countries. Since the sale of its environmental technology division at the end of October 2025, the business has been consolidated into three divisions:
Figure 2: The EcoPump GW iD is available in various models, such as one with a pressure regulator.
Automotive: painting technology, final assembly, testing and filling technology as well as production technology for battery electrodes Industrial Automation: assembly and test systems for automotive components,
medical devices, and consumer goods as well as balancing technology solutions Woodworking: machinery and equipment for the woodworking industry Visit: www.durr.com
Automated Water & Effluent Ltd Get in touch for a quote today! Automated Water & Effluent Ltd have been supplying process control equipment to the metal finishing and surface finishing industry.
CALL T O D AY O N
0 17 8 5 2 5 4 5 9 7
We have an in-house team of qualified engineers able to design and build control panels and process equipment specifically to fit your requirements. A wide range of our control instrumentation, dosing pumps and chemical process equipment is available on short delivery. • Custom Designed & Built Control Panels • pH & Redox Controllers & Electrodes • Conductivity Controllers • Liquid Level Controllers • Open Chanel & Magnetic Flow Meters • Data Loggers • Dosing Pumps & Tanks Call today for a quote or to inquire. AWE House, Antom Court, Tollgate Industrial Estate, Stafford, ST16 3AF
awe-ltd.co.uk
01785 254 597
half-page-2023-pump-up-the-volume-ad.indd 1
03/07/2023 15:53
DOWNLOAD HMG’S FLOOR PAiNT GUiDE
ONE RANGE. EVERY FLOOR. EVERY PROJECT. FROM GARAGES AND WORKSHOPS TO WAREHOUSES AND PRODUCTiON FACiLiTiES, HMG'S FLOOR PAiNT RANGE DELiVERS OUTSTANDiNG DURABiLiTY AND THE RiGHT COATiNG FOR EVERY JOB.
POLYURETHANE
FLOOR PAiNT • • • • • •
Water-based technology Suitable for concrete, walkways & steps Light industrial traffic resistance Mid-sheen professional finish Touch Dry Time: 30-45 Mins Recoat Time: 1 hour
TRADE APPROVED
2K EPOXY HD
FLOOR PAiNT
• • • • • •
Durable polyurethane resin technology Solvent-based Light to medium traffic areas Touch dry: 1-2 hours Hard dry: 4 hours Full cure: 7 days
FLOOR PAiNT
• • • • • •
Solvent-based two-pack formulation Medium to heavy traffic areas Touch dry: 1-2 hours Hard dry: 16-24 hours Full cure: 3-7 days Excellent chemical resistance
hmgpaint.com
SURFACE PREPARATION, DEGREASING & CLEANING
IMPORTANCE OF GOOD TOOLING Contact, Drainage and Flow: What Tooling Design Actually Decides Ultrasonic cleaning is a tolerant process. A great many components clean perfectly well tipped loosely into a basket, and for open geometries with moderate cleanliness requirements, elaborate tooling earns nothing. The useful question is where that tolerance ends, because when a well specified system produces an unacceptable result, the cause is frequently not the machine, the chemistry or the cycle. It is how the component was held.
Some typical Examples of carefully thought out tooling.
46
The contact point carries more conflicting requirements than any other feature of a fixture. It must hold the component securely, since a part free to move in an ultrasonic field will vibrate against its support and mark. It must do so without damaging the surface it touches, and polished, soft and coated surfaces allow very little margin. It must sit clear of optical, sealing and datum surfaces, because a contact mark on a functional surface is a scrapped part however clean the component is. It must occupy the smallest area consistent with holding the part, since whatever it covers is shielded from the process. And it must be shaped so that liquid runs off it rather than collecting in it. That last requirement is the one most often overlooked, and it is a drying requirement rather than a cleaning one.
Powder Checker
Non-contact Uncured Powder Thickness Gauge Affordably measures uncured powder coatings using non-contact ultrasonic technology to predict a cured thickness
Dedicated stand-alone unit is ready to measure right out of the box
Fast measurement speed—ideal for moving lines and swinging parts
Scan Mode continuously takes measurements—ideal for analyzing large areas
Storage of 999 readings with onscreen averaging. Stored readings can be downloaded to PosiSoft Desktop Software
Powder Inspection Kits
Complete solutions for measuring powder coating before and after cure are available 16A Long Drive, Meadway, Berkhamsted, Herts HP4 2PN t: 01442 879494 www.dftinstruments.co.uk e: sales@dftinstruments.co.uk
SURFACE PREPARATION, DEGREASING & CLEANING
Tooling designed to hold components on edge with minimal, repeatable contact, and shaped so that liquid runs off the contact rather than collecting at it.
Liquid is retained in the capillary volume at every contact point, and it exchanges with the bulk bath slowly. On withdrawal, the film draining down the component collects at the lowest contact, where the meniscus pins, so that everything dissolved across the wetted area is delivered into a single droplet. If that droplet evaporates before it drains, the dissolved load is left behind as a ring. The mechanism is the one described by Deegan and colleagues in 1997, in which a pinned contact line and uneven evaporation drive an outward flow that concentrates dissolved solids at the perimeter. The practical consequences are that a slower final lift carries a thinner film, and a smaller dissolved load, out of the bath; that drainage time before transfer is a process parameter rather than lost throughput; and that a contact geometry which sheds liquid will outperform one which cradles it. Germanium illustrates how substrate-specific this becomes. It conducts heat at around 60 W/m.K, against roughly 30 for sapphire and under 2 for fused quartz, so it can supply the latent heat of vaporisation to a pinned droplet faster than the meniscus is able to drain. A droplet held at a contact point can therefore dry in place rather than run off, fixing its residue as a ring at exactly that location, and a ring at the edge of an optic can spread far enough to encroach on the clear aperture. The same tooling, chemistry and rinse can be entirely adequate for sapphire or fused quartz on the same line. The failure in such a case is one of drainage and drying, not of cleaning, and it is invisible until a material with the right thermal properties is put through the process. Orientation relative to flow is the factor most often left to chance. Cleaning and rinsing both depend on exchanging fluid at the surface, so components should be presented edge-on to the direction of flow and agitation rather than face-on, and spaced so that each part is not sitting in the hydraulic shadow of the one in front of it. Parallel presentation allows liquid to pass between components and reach every surface; parts laid across the flow mask one another, and the ones behind are rinsed by fluid that has already been loaded by the ones in front. The same reasoning rules out stacking and nesting, where a part sits
48
inside another and no amount of bath power will reach the enclosed volume. Fixture and basket material matters more than is generally recognised. Polymers are viscoelastic: they dissipate acoustic energy as heat in a way that bare metal does not, so a coated or heavily plastic-bodied basket absorbs energy that would otherwise be available in the tank. The decisive barrier, though, is air. Water and air differ in acoustic impedance by a factor of several thousand and reflect virtually all incident energy at the boundary, so a foamed liner, a porous coating or a bubble clinging to a surface behaves as an acoustic mirror. The same physics applies inside the component, because cavitation occurs only in liquid: air trapped in a blind hole is a region of no cleaning at all, and increasing generator power will not change it. Orientation that lets air escape on immersion, and lets liquid drain on withdrawal, is worth more than power. Scale is worth keeping in view, since at 40 kHz the wavelength in water is around 37 millimetres, so a fine basket wire is a far smaller obstruction to the field than a solid sheet, a stacked load or a lined container. Tooling therefore earns its cost in three circumstances: where geometry can trap air, mask a surface or allow parts to nest, which is a physical failure that power cannot correct; where the substrate or finish is vulnerable to contact marking or to drying residue, which includes polished surfaces, soft metals and optical components; and where the cleanliness requirement must be demonstrated rather than judged acceptable by eye. Where those conditions apply, tooling is a process variable and belongs in the process design rather than in the purchase order. Unitech Shyre designs and manufactures custom tooling and part jigging alongside the machine, the process and the chemistry, with trials run on the customer’s own components before commitment. Unitech Shyre Ltd designs, manufactures and supports automated precision cleaning, dip coating and fluorescent penetrant inspection systems for the optical, ophthalmic, medical, semiconductor, aerospace and precision engineering sectors. www.unitechshyre.co.uk
FOR ALL YOUR VIBRATORY FINISHING EQUIPMENT AND MATERIALS New and used vibratory finishing machines and systems from 2 litres to 4000 litres Finishing media; Ceramic, Plastic, Wood, Steel and Maizorb Liquid / powdered / paste compounds Abrasive finishing wheels Vibratory separators / sieving machines and re-meshing service Repairs and relines Effluent water treatment systems Subcontracted finishing and industrial sieving services Redundant machines purchased Consultancy
SHARMIC FOR FAST, FRIENDLY SERVICE Experienced Engineers After sales technical support Nationwide deliveries
Sharmic Engineering Ltd Tel: +44 (0)1299 822135 / 878123/4/5 Email: info@sharmic.co.uk www.sharmic.co.uk
SURFACE PREPARATION, DEGREASING & CLEANING
STOP PAYING FOR PROBLEMS YOU COULD HAVE PREVENTED Why Reactive Maintenance Costs Precision Cleaning Operations - More Than You Realise A precision cleaning process rarely fails all at once. Performance drifts gradually: solvent quality declines, contamination rises, and machine parameters shift. By the time production issues like increased rework, failed inspections, or unplanned downtime appear downstream, the financial damage is already done. For many manufacturers, the root cause isn’t the aqueous or solvent equipment, it’s the absence of structured process ownership.
The Hidden Cost of Supplier Fragmentation In the precision cleaning sector, equipment, chemistry, servicing, and waste handling are typically managed by different suppliers. This fragmentation of responsibility means problems are treated reactively rather than prevented systematically. Reactive maintenance creates a cycle of disruption: Unexpected breakdowns interrupt manufacturing schedules. Process drift leads to inconsistent cleaning and rework. Emergency interventions drive up service costs. Solvent degradation reduces cleaning efficiency Most of these disruptions are preventable. When these elements are managed through a single, structured lifecycle programme, cleaning becomes predictable, repeatable, and reliable. A structured preventative maintenance programme removes variability before it impacts production.
Closing the Market Gap: From Supplier to Process Partner The industry has traditionally suffered from a “disconnected supply” model: one vendor for equipment, another for chemistry, and a third for waste. No single provider takes ownership of the entire process. Fraser Technologies addresses this gap. We move beyond simple distribution to support the complete cleaning lifecycle. Our objective is simple: Maximum uptime. Minimum surprises.
50
The Fraser Technologies Maintenance Programme The Fraser Technologies Maintenance Programme is designed to move manufacturers away from reactive problem-solving and towards proactive process control. A structured service framework maintains cleaning stability at every stage and covers all precision cleaning equipment types (aqueous, solvent, ultrasonic): Process Audits: Verifies optimal conditions to avoid performance drift early. Preventative Maintenance: Ensures long-term equipment reliability via scheduled interventions. Solvent Testing & Stabilisation: Prevents chemistry drift before it reaches your parts. Planned Service Interventions: Operational disruption minimised due to consistent system tuning. Integrated Waste Management: Environmental compliance always met due to streamlined handling. Each element reinforces the others. The result is a controlled, stable, high-performance cleaning process with significantly reduced operational risk.
framework including process optimisation, chemical maintenance, and responsive UK-based technical support. This isn’t just equipment servicing; it is complete process control.
Zero Unplanned Downtime Starts With Control High-performance cleaning is achieved through planned maintenance and expert management. Manufacturers adopting this integrated approach benefit from: Stable, repeatable cleaning outcomes. Maximum equipment uptime and extended solvent life. Lower total cost of ownership. Improved compliance and operational confidence. Not Just a Supplier. Your Cleaning Process Partner. Fraser Technologies takes ownership of performance long after installation. By integrating equipment, chemistry, maintenance, compliance, and optimisation into a single managed framework, manufacturers gain something increasingly valuable in modern production environments:
Built-In Reliability for Vacuum Degreasing
Process certainty.
Specifically for vacuum degreasing systems, Fraser Technologies offers the deepest level of support within this broader servicing programme, by delivering a fully integrated
To find out how the Fraser Technologies Maintenance Programme can eliminate cleaning variability in your operation, visit www.frasertech.co.uk or speak directly to our technical team on 01506 443058.
SURFACE PREPARATION, DEGREASING & CLEANING
The challenge: Shot blasting of large components
FRENCH SUPPLIER OF REFUSE COLLECTION VEHICLES PLACES HIS TRUST IN RÖSLER’S BLAST CLEANING COMPETENCE The French SEMAT SA is a subsidiary of the German Zoeller group of companies and specializes the design, production and servicing of RCV and street washers’ vehicles. SEMAT, founded in 1945, is headquartered in La Rochelle, a town on the Atlantic coast. There, the company recently erected a new manufacturing building filled with state-of-the-art industrial equipment. The central feature is an indexing continuous feed spinner hanger blast machine, model RHBD-T, from Rösler. In the new building in La Rochelle bodies are welded together from steel sheets and subsequently prepared for coating. The surface preparation consists mainly of the removal of scale from the welding process but also rust. This is a typical blast cleaning operation, one of numerous shot blasting tasks. Because the components to be blast-cleaned are really big, the SEMAT project was particularly challenging. For example, the welded bodies for garbage trucks can be up to 6,500 mm high and 4,000 mm wide. Ronny Paasche, global sales expert at Rösler explains: “Initially we discussed several different options. But we decided very quickly that a continuous feed spinner hanger blast machine represented
52
SURFACE PREPARATION, DEGREASING & CLEANING
the best solution. It allows the customer to blast his large components within short cycle times with a high degree of efficiency and a relatively low energy input. And, compared to classical continuous blast machines, vertical processing saved a considerable amount of space.” In this case “vertical” means that the components are transported into the blast chamber upright for an all-around blast coverage. But it was not only the compact equipment design that convinced SEMAT to buy the blast machine from Rösler. Ronny Paasche continues: “The customer was particularly impressed by the numerous technical features, which are part of our standard equipment but are considered as state-of-the-art in the market.”
Gamma 400G turbines offer a maximum of blasting power at relatively low energy consumption Depending on the preceding manufacturing steps, the rust and scale on the components can be extremely hard, requiring intense “firepower” by the blast media. This is guaranteed by nine Gamma 400G turbines mounted on one wall of the blast chamber of the RHBD-T machine. The work piece, hanging on
54
a special fixture that constantly rotates and oscillates back and forth, is exposed to the blast stream of the nine turbines. This ensures excellent, all-around blast results. And thanks to their innovative, energy-saving design, the Gamma turbines only need a power of 11 kW per unit. But since they accelerate the blast media to a comparatively very high throwing speed, the Gamma turbines produce optimal results. After a cycle time of about 10 – 15 minutes the containers leave the blast machine completely clean with a cleanliness degree of 2,5 SA – ready for transport to the painting line. A manual control system allows calling up about 30 different blast programs so that blasting time and intensity can be adapted to the special processing challenges of each individual container. Therefore, the cleaning results are highly consistent, even though the raw work pieces may not always have the same surface conditions when entering the blast machine.
Optimal media recycling and cleaning guarantees high costefficiency and sustainability A pre-condition for economic and sustainable shot blasting operations is a highly efficient blast media recycling and cleaning system. The center of a well-functioning media cleaning system
“The Professionals”
EST 198 . 9
Sub contract specialists in Paint & Powder coat removal to the finishing industry JIG CLEANING PAINT BOOTH GRID CLEANING COMPONENT RECLAMATION
Save up to 20% on your “monthly stripping costs ” Send your enquiry today!! email info@prostrip.co.uk web www.prostrip.co.uk phone 0115 911 2240
Pro-Strip Ltd. Trent Lane, Daleside Road, Nottingham NG2 4DS
SURFACE PREPARATION, DEGREASING & CLEANING
is the cascade air wash separator. Compared to competitive equipment the air wash separator in Rösler blast machines is considerably wider and, thus, guarantees a more thorough cleaning effect for the media. “The extra wide air wash separator permits a very thin media curtain ensuring that contaminants, such as debris, broken down media, etc., are consistently removed from the blast media”, explains global sales expert Ronny Paasche. “Contaminants left over in the media recycling system will damage the throwing blades, the lining of the blast chamber and even the work pieces. Thanks to our extra-wide, highly efficient air wash separator we have, therefore, significantly less wear and tear in the shot blast machine. Particularly scale particles can be extremely abrasive and must, therefore, be completely removed from the media.” An additional benefit of the extra wide air wash separator is the reliable discharge of undersized blast media. Because the excellent cleaning system in the Rösler machine results in a better media classification, it also helps reduce the overall media consumption. Especially helpful in the case of the SEMAT machine was the fact that the air wash separator is located 10 meters above ground. It allowed installation of a flap screen that automatically discharges foreign objects such as screws, flash, etc., from the media recycling system. Emptying the screen is controlled by a timer. Other technical details in the SEMAT blast machine ensure that the entire blast cleaning operation can be performed safely and effectively. For example, a media return hopper covered by a sturdy
grate is built into the floor at the machine exit. This guarantees that the machine operator can remove any residual media from the cleaned work piece without the risk of slipping on blast media lying on the floor. A special auger transfers the collected residual media back to the media recycling system.
Effective dust removal guarantees maximum uptimes Another extremely important consideration for the economic operation of a shot blast machine is the effective dust removal from the blast chamber. In the SEMAT machine the air stream loaded with dust is initially guided to an expansion chamber, a so-called dropout box, containing an impact plate. There, particles too small for the shot blast process but too big for the dust collector, are discharged. Only very fine particles are transferred to the dust collector. This extends the usable life of the dust collector and the uptime of the filter cartridges. The air extraction volume is calculated on the basis of computer-based air flow simulations, which have become standard procedure at Rösler. This ensures that after it has been cleaned in the air wash separator, the blast media contains no dust residues whatsoever, ready for the next blast cycle. The work pieces coming out of the blast machine must be completely free of dust so that their surface provides perfect conditions for the subsequent coating operation.
Safe, sturdy and easy to maintain: The SEMAT blast machine fulfills all expectations In many companies the blast cleaning operation of large weldments is still done manually. But the industry is slowly phasing out large, inefficient blast rooms, where the components are manually cleaned with extremely expensive compressed air. In comparison to these
56
manual operations the advantages of the spinner hanger blast machines are quite obvious: Manual blasting of large components requires processing times that – compared to machine blasting – are multiple times longer. Personnel for this physically demanding job is difficult to find. At the same time, the compressed air usage and, thus, the energy consumption is very high. Automated, mechanical systems offer a much higher capacity, are more economical and produce absolutely consistent results. Ronny Paasche from Rösler concludes: „Recently we delivered a blast machine similar to the SEMAT system to another customer. With this machine our positive experience from the project at SEMAT was extremely helpful. We are pleased that our innovative approach to challenging shot blasting tasks is helping us to secure new business.“ For over 90 years, the privately owned Rösler Oberflächentechnik GmbH has been actively engaged in the field of surface preparation and surface finishing. As a global market leader, we offer a comprehensive portfolio of equipment, consumables and services around the mass finishing and shot blasting technologies for a wide spectrum of different industries. Our range of about 15,000 consumables, developed in our Customer Experience Centers and laboratories located all over the world, helps our customers to fulfill their individual finishing requirements. Under the brand name AM Solutions, we offer numerous equipment solutions and services in the area of additive manufacturing/3D printing. Last but not least, the Rösler Academy, our central training center, offers practical, hands-on seminars on the topics mass finishing, shot blasting and additive manufacturing. The Rösler group has a global network of 15 manufacturing operations and sales branches as well as 150 sales agents. For detailed information please go to: https://facts.rosler.com/SEMATShotBlasting-Machine
SURFACE PREPARATION, DEGREASING & CLEANING
New Focus of Karl Roll – high cleaning quality with low throughput
COST-EFFECTIVE SOLVENT CLEANING WITH FOCUS ON WHAT MATTERS MOST The new Focus plant is the Karl Roll´s answer to the altered demands in the parts cleaning. This cost-effective solvent cleaning plant features all the essential equipment details to meet high cleanliness standards reliably, cost-effectively, and in a way that conserves energy and resources, even when the volume of items to be cleaned is relatively low.
The transformation processes in the industry lead to changes in the parts cleaning. As a result, an increasing number of industries are finding themselves having to clean smaller quantities more frequently, while at the same time meeting higher cleanliness standards. The cleaning not only has to be reliable and reproducible but also very economically and resource-efficient. For this assignment Karl Roll has developed the new Focus. This costeffective closed-loop solvent system impresses with an excellent value for the price and allows an entry in the high-quality component cleaning even on a limited investment budget. The compact cleaning plant takes up very little space and requires only an industrial power supply and a compressed air connection. The Focus operates under full vacuum and can be used with hydrocarbons or modified alcohols. The working chamber can take loads with the dimensions of up to 565 x 365 x 250mm and a weight of maximum 50kg.
Features designed for a high level of cleanliness are included as standard
The Focus was developed to meet changing requirements in parts cleaning. This cost-effective solvent cleaning system ensures a high level of cleanliness even with a relatively low cleaning volume.
58
In designing the new plug-and-play solution, the equipment manufacturer has integrated everything as standard features to ensure that high cleanliness specifications are achieved in a processstable and repeatable manner. These include, among other things, two solvent tanks with separate media circulation systems and bypass filtration. These can be used for pre cleaning and fine cleaning when very high cleanliness standards are required. Alternatively, it´s possible to use the first tank for cleaning and the second one for conservation.
The solvent cleaning plant has two flooding tanks with separate media cycles as a standard. One of these tanks can be used for conservation. In both cases, two powerful pumps ensure rapid emptying of the working chamber. Furthermore, the plant has ultrasound integrated. The frequency can be adjusted company-specific. A loading aid ensures ergonomic working conditions. At the customer’s request, the loading aid can be expanded to an automatic loading and unloading system.
A barcode scanning system is available as another option for unmanned operation.
Aggregates and processing for energyand resource-efficient operations
The standard equipment also includes ultrasonic elements in the working chamber. They help ensure that high cleanliness standards are met in a reliable, reproducible, and resource-efficient manner.
To keep operating costs as low as possible, special attention was paid to low energy consumption when selecting system components such as vacuum pumps, heaters, and drain pumps. This results in an optimum ratio of power to consumption. Furthermore, the plant has, like every solvent cleaning plant of this manufacturer,
an integrated distillation unit for the continuous processing of the solvent. The distilled oil is continuously removed via an automatic oil discharge system, so the solvent remains free of residual oil for a very long time. This significantly extends the service life of the cleaning medium. In addition to the energy efficient aggregates, the use of the heat from the distillation unit and the effective insulation of all heated media are key factors contributing to the plant’s energy-efficient operation. Detached particulate contaminants are removed by a filter unit. To prevent solvents from escaping into the environment during manual filter changes due to an improperly sealed filter housing, the system can be equipped with an automatic lid lock upon request. By focusing on the essential equipment features required to meet high cleanliness standards, the cost-effective Focus solvent cleaning system sets new standards for cost-effectiveness and resource consumption when dealing with low cleaning volumes. Its excellent value for money also makes this cleaning system an ideal solution for the demanding cleaning of small parts. www.karl-roll.de
59
PAINT & POWDER
WHY PROTECTIVE COATINGS AND FLOORING ARE FOUNDATIONAL STADIUM CONSIDERATIONS In 2026, stadiums are taking centre stage, with major sporting events such as the football World Cup drawing crowds in their tens of thousands to enjoy the spectacle and soak up the atmosphere. Operators, on the other hand, are fully focused on keeping people safe and venues ready for the global spotlight – and that means factoring in foundational project elements, such as protective coatings and flooring, from the very start. The modern world demands a lot from stadiums. They need to stand up to eye-watering volumes of footfall, provide clear sight lights and an exciting atmosphere, all while remaining clean, safe, and aesthetically pleasing. And they need to deliver all this repeatedly, often across back-to-back events, which makes structural integrity, public safety, operational resilience, and a broadcastready appearance non-negotiable. As stadium owners and operators prepare for a new era of global sporting events, the pressure is on to deliver venues that are safe, durable, visually impressive, and ready to perform under intense public scrutiny. These are not straightforward projects. Teams are working to strict deadlines, with no margin for error, to ensure venues are completed and operational ahead of planned events. Protective coatings and flooring are a foundational element of the overall equation, providing functions such as fire and corrosion protection, slip resistance,
60
aesthetics and wayfinding. Yet despite being part of the very fabric of the building, decisions around them are often left too late. The results are missed completion deadlines, the need to close down and re-do work later on, and, ultimately, missed opportunities.
environments, 2-pack epoxy technology provides ultimate durability and weather resistance, while 1-pack solvent-based solutions are key cost-effective and efficient solutions and water-based solutions can help support lower VOC requirements.
Complex considerations
Exposed structural elements also need protection against the electrochemical process that lead to rust. Specialist anti-corrosion coatings shield steel from the surrounding environment, mitigating the risk. With the required coating specification being dependent on exposure levels, however, determining product and application needs can be challenging. ISO 12944, the industry standard for corrosion protection of steel structures by protective paint systems, classifies need based on factors such as location, use, and atmosphere. What complicates things further is that one stadium could fall into multiple ISO 12944 categories. While offices and canteens, for example, may be C1, or very low risk, outdoor spaces like the arena may be C5, or very high risk, especially if in a coastal area. Selecting a coating system that aligns with the relevant ISO 12944 environment classification is critical to achieving long-term corrosion protection and reducing maintenance requirements.
Stadiums are unlike any other infrastructure project. They operate like a small town, with tens of thousands of people attending at any one time, and dozens of different areas with different uses. As such, corrosion and fire protection, as well as flooring requirements, have to be individualised to the project. Stadiums need passive fire protection for steel structures and load-bearing elements. When exposed to extreme heat, intumescent coatings form an insulating layer that protects the steel for a specified period of time. In the event of a fire, this ensures structural integrity during the evacuation of a stadium-sized crowd. However, there is no-one-size fits all solution to passive fire protection, and intumescent coating specification has to be performed as part of a broader system approach. The correct technology for your project will depend heavily on factors such as regional regulations and the size of the stadium, the desired speed of evacuation and the volume of exposed steel, as well as the project-specific needs for durability and method of application. Intumescent coatings have various chemistries designed to meet a wide range of project requirements. Multi-component methyl methacrylate (MMA) technology, for example, offers an advanced, ultra fast-curing in-shop applied and durable solution for passive fire protection. In C4 and C5
Behind every stadium is a complex network of mechanical, electrical and plumbing services that keep the venue operational. Corrosion under insulation (CUI) on pipework and thermal systems can remain undetected for years, increasing maintenance costs and operational risk. Protecting these critical assets helps ensure reliability, uptime and long-term performance. High heat coating solutions help protect piping and mechanical systems from corrosion, extreme temperatures, and operational risks, reducing maintenance and extending asset life.
Flooring decisions come with equally complex considerations. Each one of the multitude of different areas that make up a stadium will have different needs and considerations. Selecting the appropriate system for each zone can reduce maintenance costs while supporting smooth venue operations throughout the asset lifecycle. Flooring systems also contribute to public safety, cleaning efficiency, and asset longevity. Resin floors are seamless, polymer-based surfaces which are applied in liquid form directly to a prepared surface and cure chemically to form a durable, abrasionresistant finish. The chemistry and thickness of the system will dictate its performance, such as cleanability, the types and volume of traffic it can manage, and slip resistance. A locker room or a concourse, for example, will have very different flooring requirements to a car park or a delivery bay.
What’s more, different flooring systems have different application and drying times. If this is not factored in from the start, it can lead to unexpected delays. Opting for a fast-drying solution means minimal downtime and a faster path to project completion.
requirements, lower emissions during application, and support for green building certifications such as LEED and BREEAM. Selecting durable systems at the design stage can help reduce lifecycle costs while supporting environmental goals throughout the life of the venue.
Another common consideration is colour scheme and way finding. Venues will have very exacting requirements regarding the finished look of the stadium, often aiming to reflect brand or corporate colours. As aesthetic and directional colours are applied over the top of coatings and floorings, making sure they are compatible up front will save headaches and delays later on in the project.
Strong foundations
Modern stadium projects are increasingly being designed around sustainability objectives. Protective coatings and flooring systems can contribute through longer service life, reduced maintenance
Understanding the right approach for your stadium, then, is incredibly complex. But these are foundational elements of the structure, and if they are not considered and planned from the start, they can hold up the entire project. That’s why protective coatings and flooring should be built into venue design from the very beginning. It is about ensuring public safety, enhancing operational resilience, and minimising expensive delays. https://industrial.sherwin-williams.com
61
PAINT & POWDER
THE FARADAY CAGE: WHY “ELECTROSTATIC” SOLUTIONS FAIL IN RECESS COATING By Sergey Guskov, Nordson Corporation In my 35 years in the powder coating industry, perhaps the most frequently used term to describe a challenging application is the “Faraday Cage effect.” It’s named after Michael Faraday, the British scientist who in 1836 demonstrated that external electric fields do not get through a grounded metal cage. In modern powder coating, it has become common to refer to almost any recessed or corner area as a “Faraday cage area”. But is this term correctly applied? Is there indeed no electric field inside the corners or recesses of the products we coat? The short answer is a resounding “No.” The term is not only wrongly applied in our industry, but it is also misleading. By labelling these challenges as “Faraday Cages,” we wrongly point users toward an electrostatic phenomenon. This suggests that improving the coating of complex shapes should be addressed by managing the electric field and charge. Equipment suppliers often take advantage of this misconception and the fact that we plainly can’t see electric fields by claiming that a new electrostatic control in a spray system can magically “break into” these areas. Unfortunately, that is often just smoke and mirrors.
electric field is created between a thundercloud and the ground resulting in lightning, this second field—called the “space charge” field—exists everywhere charged particles are present. Figure 1
The Invisible Wall: Aerodynamics If there is an electric field inside the recess, then the term “Faraday cage” is clearly being used incorrectly. It also means that trying to improve coverage solely by tweaking electrostatic parameters might not be the right approach.
Electric Field – Is There Only One? Most of us recall from school an image of an electric field depicted as lines between two electrodes. Figure 1a illustrates the field between the charging electrode of a spray gun and a grounded object. However, this picture changes once a corona discharge develops and we start spraying powder. As soon as the space between the gun and the part is filled with charged air molecules, ions, and powder particles, a second electric field is created by the cumulative charge of that cloud. Figure 1b. Much in the same way an
62
This space-charge field is absolutely essential for powder deposition. Without it, gravity or aerodynamic forces would simply overpower the process, and the desired coating layer would struggle to form. No matter how small or narrow a corner is, if a spray system delivers a cloud of charged powder inside that recess, that cloud creates its own electric field.
As shown in Figure 2, the external electric field created by a spray system follows the path of least resistance to the nearest surface which is often the edges of a recess. Thus, if a spray system is positioned some distance away from a product we powder coat (as is the case with most automatic powder coating systems) there is no help from the external field in the deposition of a coating layer inside recesses.
Outstanding Powder Coating Performance
Advanced Automation and Color Change • • • • • •
Superior coverage and process control for significant powder savings Fast, reliable, highly automated color change with visual access Advanced automation solutions for reduced manual coating High finish quality with advanced charge control and ultrasonic sieving Industry 4.0 ready IO links User-friendly, connected controls with visual guides and help content
www.nordson.com/powder ics.eu@nordson.com
ive es
hin
ac tm
as
bl
Built for durability, designed to deliver.
as
br
ya
dr
Abrasive Blast Equipment
| pr n
isio ec
Elcometer’s CONTRACTOR and PERFORMANCE abrasive blast equipment is engineered to operate at maximum efficiency for better performance.
ia
ed
m s|
lve
va e os th as bl
s|
b Surface World - Ella.indd 1
o
tn
s la
le zz
n tio c te ro p l na sr o pe
t en m uip q e
BLAST IT elcometer.com
12/05/2025 07:44:55
PAINT & POWDER
Figure 2
Figure 3 shows a coating application on a garage door having narrow recesses on its surface. Only the field of the space charge exists inside those narrow channels. In a closed recess (Figure 4.), the airflow from the spray gun creates massive aerodynamic turbulence. The real hurdle in recess coating is a dramatic interplay between electric and aerodynamic forces. When a spray system targets a closed recess or corner, the air used to transport the powder creates significant turbulence. If this air moves too fast, it acts as an invisible barrier, disrupting the powder deposition process before the electric field can do its work.
The Vicious Cycle of High Velocity: When the spray velocity is too high, operators often fall into a counterproductive cycle: The Over-Spray Loop: You keep spraying to force coverage, but the high-velocity air continues to blow the powder out of the recess. Figure 4
Figure 3
Back Ionization: This continuous spraying leads to the development of back ionization on the outer surfaces. Charge Deterioration: These outer surfaces emit positive ions that can attach to negatively charged powder particles reducing their charge and weakening the “space charge” field inside the recess. Deposition becomes even more difficult. The end result is a poor-quality finish, excessive powder buildup on the edges and insufficient coverage in the corners. Historically, coaters are advised to simply reduce the high voltage to improve coverage. While lowering voltage can delay the development of back ionization, it is a double-edged sword. Setting the voltage too low reduces the strength of the electric field between the gun and the part, leading to a lower charge on the powder cloud. This actually weakens the essential space charge field inside the recess and does nothing to solve the underlying aerodynamic problem.
The Solution: Slow down to speed up To overcome the negative influence of air turbulence, we have to change how we deliver the powder. In systems using traditional venturi pumps, slowing down the spray pattern is difficult. Because these pumps use standard 10–11 mm diameter hoses, they require a high volume of air just to transport the powder to the gun. This excessive air inevitably leads to higher spray velocity and more turbulence. The real breakthrough came with the introduction of HDLV (High Density Low Velocity) pump technology. Figure 5. Unlike venturi systems, HDLV uses dense-phase technology where “powder is pushing powder” through a much narrower 6 mm hose. This allows coaters to control the spray velocity completely independently of the powder output by adding the pattern air directly to the spray gun and not at the pump. Soft Spray Patterns: HDLV creates a gentle powder cloud that reaches into recesses without the “bounce-back” caused by high-velocity air.
64
Figure 5
High Efficiency at High Output: You can deliver more than 450 g/min of powder while maintaining a “soft” cloud, ensuring high application efficiency even on the most complex geometries. Reduced Turbulence: By eliminating the excess transport air, the aerodynamic chaos inside corners is minimized, allowing the space charge to do its job in assisting the powder deposition.
The Perfect Match: HDLV and Robots In recent years, the powder coating industry has seen a steady increase in the use of robot automation, especially on complex products that usually demand extensive manual touch-up. A properly set-up robot can do all an operator does, but faster and with greater process control. I’ve spent years training spray operators, and I have so often advised them to keep the gun farther away to achieve a slower spray pattern for better efficiency. Yet, if I have a spray gun in my hand and a deep cavity in front of me, there is no force that will keep me from sticking the gun into a recess. Such is our human nature.
Repeatability: Robots are 100% repeatable. HDLV pumps deliver constant output for thousands of hours without needing adjustments to compensate for wear. Targeted Positioning: Robots bring spray systems close to their target area. Because HDLV delivers a soft spray pattern, it enables this close-in application without creating excessive aerodynamic turbulence. Moreover, when a spray system is moved close to a challenging corner, its external electric field also moves inside working together with the field of the space charge to significantly increase the deposition efficiency. Figure 6 shows a system with 4 robot mounted spray systems which replaced 16 venturi spray systems delivering much higher efficiency and finish quality at the same production rate. Moreover, by applying powder at close distance to challenging corners, the coating thickness on the external surfaces is greatly reduced for significant applied coating savings.
Conclusion: Moving Beyond the Myth Successful powder coating is about achieving a delicate balance between electrostatics and aerodynamics. When we stop blaming the “Faraday Cage” for
every challenging corner, we can finally address the true culprit: the air velocity that inhibits powder deposition. By shifting the focus from high-voltage and electrostatics to controlling the spray velocity, we move from guesswork to a reliable, scientifically sound powder coating application. As our industry continues to embrace automation and robotics, the choice of application technology becomes even more critical. Embracing HDLV technology doesn’t just solve a technical hurdle, it empowers your operators (and your robots) to deliver superior finishes, faster and with lower powder waste. After all, the goal isn’t just to fight through a perceived “cage,” but to use the smartest tools available to ensure the powder goes exactly where it belongs.
About the Author Sergey Guskov is a Sales Manager for Industrial Coating Systems at Nordson Deutschland GmbH. A veteran of the powder coating industry since 1989, Sergey holds a Dipl. Ing. in Electrical Engineering and an MBA. His diverse career spans R&D in high-voltage technology, engineering, marketing, and sales management. Visit: www.nordson.com
Figure 6
With dense-phase technology, there is no more need to fight that nature. Whether it is an operator with a hand gun or a spray system mounted on a robot, you can work very close to the target corners without blowing powder off. There is a unique match between the capabilities of robots and HDLV spray systems: High Output with High Efficiency: Robots move fast and require high powder output. HDLV systems can deliver more than 450 g/min without losing application efficiency.
65
MATERIAL & EQUIPMENT SUPPLIERS ABRASIVE BLASTING EQUIPMENT
ABRASIVES
Steel Shot (High & Low Carbon) Steel Grit Stainless Steel Shot and Stainless Steel Grit (Cr & Cr/Ni) Chilled Iron Grit Glass Bead Ceramic Bead Fused Alumina Cut Wire www.ampereabrasives.com sales.uk@ampereabrasives.com Tel : 0121 244 1809 17 School road, Hall Green Birmingham B28 8JG
No 5, Queensway Link Industrial Estate Stafford Park 17, Telford, Shropshire TF3 3DN Tel: 01952 299777 Fax: 01952 299008 E-mail: sales@pometon.co.uk
ACIDS
BOILERS & STEAM GENERATORS
ANODES & CHEMICALS
ELECTROPLATING
High Carbon Steel shot and Grit. Low Carbon Steel Shot and metal Bead Stainless Steel Cr and Cr/Ni.
ANODES & CHEMICALS
www.ampere.com sales.uk@ampere.com Tel : 0121 244 1809
17 School Road, Hall Green, Birmingham B28 8JG
COMPLETE FINISHING PLANT
MACHINERY
Modern Coil Type Steam Generators & Fire Tube Boilers • • • • • •
100Kg/h – 25,000Kg/h High efficiency – up to 96% Low overall emissions Improved safety Simplicity of control Quiet, clean & cool in operation
Tel: 020 8953 7111
• PLANT CONTROL SYSTEMS • DATA MANAGEMENT SYSTEMS • BARRELS - PROGALVANO ROTOR • BARREL AUTO LOADING SYSTEMS • PROGALVANO FILTERS • SEMI/AUTOMATIC FILTER SYSTEMS • CENTRIFUGAL DRYERS (Large Range) • AUTOMATIC DRYING SYSTEMS • ROTARY PAINTING/LAQUERING • TOP COATING/SEALING SYSTEMS • VIBRATORY POLISHING EQUIPMENT • LUBRICATION EQUIPMENT • RECTIFIERS Conventional & Pulse • A/HOUR METERS & DOSING PUMPS
• Ovens • Spraybooths • Pre Treatments • Paint Mix Room • Full Turnkey • Servicing & Maintenance
Specialists in Spraybooth & Paint Finishing Solutions
info@babcock-wanson.com www.babcock-wanson.com
COATING SERVICES
Curtiss-Wright Surface Technologies, Everlube products & Coating Services Protection & life extension of your critical components throughout any crisis!
COATING SERVICES: l Thermal Spray & HVOF Coatings l Dry film lubricants - MoS2, PTFE, Graphite, WS2 l Coatings for corrosion, chemical & environmental protection l Titanium anodising l Zinc rich coatings for corrosion protection l Impingment coating processes for ultra thin solid film lubricants l Nonstick/release coatings for low coefficients of friction
l Primers for rubber and plastics for sound absorbing and dampening materials l High temperature resistant coatings l Rare earth magnet coatings l Coatings for EMI/RFI shielding provide highly conductive coatings and platings to control electromagnetic interference l Ultra thin conformal parylene coating to reduce friction and protect against contamination l Pre-treatments including Ti Anodising, Phosphate Conversion Coating and Chilled Iron Blasting, Aluminum Oxide Blasting and Vapour Degreasing
Coating Services and Everlube Products ®
+44 (0)1386 425758 | eurosales@cwst.com | www.emcoatingsuk.co.uk
66
MATERIAL & EQUIPMENT SUPPLIERS CLEANING, DEGREASING & PRETREATMENT Equipment +Chemistry + Support =
Kemet
Total Cleaning Solutions
WASHING SYSTEMS Leading Industrial Washing Machine Manufactures
“Where Hygiene Matters”
• Tray Washers • Boot Washers • Chemical Products • Crate Washers • Industrial Part Washers • Pallet Washers • Pan/Utensils Washers • Rack/Trolleys Washers • Sanitising Tunnels • Tote Bins/Buggy Washers
Tel:01543 224608 | Email washers@unitech.uk.com
DC 3505 VIXEN Dust Ad 1.qxp_Layout DUST EXTRACTION
✓ Over 50 years expertise ✓ New generation chemistries & equipment ✓ Superior performance & results ✓ FREE audit & trial facilities ✓ Extremely eco-friendly, safe and reliable
Final Cleaning • Spray Wash In-process Cleaning Aqueous Ultrasonics Precision Cleaning • FPI Lines Degreasing • Anodising Chemical Cleaning for MRO Chemical Etching/Milling
01506 443058 www.frasertech.co.uk
turbex.co.uk
E sales@turbex.co.uk T 01420 544 909 F 01420 542 264
EFFLUENT TREATMENT
For all your precision cleaning needs www.kemet-cleaning.co.uk cleaning@kemet.co.uk 01622 755287
EFFLUENT TREATMENT PLANT
GET IN
TOUCH Dust Extraction Equipment • Self Cleaning Cartridge Filters • Made in the UK • Many Sizes Available
www.neutralac.co.uk
TENNANTS
TENNANTS DISTRIBUTION LIMITED
FILTERS
PAINT STRIPPING
• EXTENSIVE RANGE OF FILTER SYSTEMS • AUTOMATIC FILTER SYSTEMS • SEMI AUTOMATIC FILTER SYSTEMS • BAG FILTERS • CARTRIDGE FILTERS • DISC FILTERS • OIL SEPARATION • FILTER PRESSES • CARBON UNITS • PUMPS • PLANT CONTROL SYSTEMS • DATA MANAGEMENT SYSTEMS
HOOKS & JIGS
67
MATERIAL & EQUIPMENT SUPPLIERS MASKING
ELECTROPLATING EQUIPMENT
OVERHEAD CONVEYORS
EQUIPMENT FOR: ANODIZING CLEANING ELECTROPLATING AND WASTE WATER TREATMENT PLEASE CONTACT LOCALLY:
TEL: 01420 544909 EMAIL: SALES@TURBEX.CO.UK LACQUERS
CHEMICALS
PRETREAMENT CHEMICALS PRECISION CLEANING & OXYGEN LEVEL CLEANING
Aluminium Anodizing Chemetall’s Anodizing Technology.
Shyre Precision Cleaning Specialists Unitech Shyre we’re leading in developing and delivering specialised cleaning processes and equipment to the precision optical industry.
OVENS
CM-WP-0377EN-07.2022
MACHINERY
Specialists in Spraybooth & Paint Finishing Solutions
Cleaning is a manufacturing process, not an afterthought. MACHINE, PROCESS, CHEMISTRY SYNERGY BY DESIGN, MADE IN THE UK, SUPPORTED WORLDWIDE
www.chemetall.com www.unitechshyre.co.uk | 01543 224531 | info@unitechshyre.co.uk
PUMP & FILTRATION SPECIALISTS
RECTIFIER EQUIPMENT
DC 3505 VIXEN Ovens Ad 1.qxp_Layo
Modular
Incubators & Industrial Ovens
GET IN TOUCH
• 100+ Models Available • Made in the UK & EU • Prices Starting from £300
Reliable Since 1935
Contact one of our UK partners
• ADVANCED MODULAR RANGE • SWITCH MODE UNITS • SCR RECTIFIERS • PULSE RECTIFIERS • RAMP CONTROLLERS • PROCESS PARAMETER PRINTING • SPECIAL COMPUTERISED RECTIFIERS • OPERATOR GUIDANCE SYSTEMS FOR ANODISING & PLATING • A/HOUR METERS & DOSING PUMPS • METERS • SHUNTS • PLANT CONTROL SYSTEMS • DATA MANAGEMENT SYSTEMS
To advertise in these pages under an existing heading or one of your own choice please call Nigel on 01442 826826 or email nigelbean1@aol.com 68
MATERIAL & EQUIPMENT SUPPLIERS POWDER COATING EQUIPMENT
DC 3505 VIXEN Powdercoating Ad 1.qx
GET IN
Powder TOUCH Coating Equipment gemapowdercoating.com
Innovative coating technology for perfect surfaces.
• Most Advanced on the Market • ROMER Unit RRP £3995 • Special OFFER Price £3495
Robotic coating
“Smart Solutions for Powder Coating’’ Serkan Inci Mail: serkan.inci@electron.com.tr Phone: +90 531 930 37 03
Your global partner for high quality powder coating
PUMPS
Powder coating
Liquid coating
SPRAY GUN WASHERS
SOLUTEX Gema Europe SRL UK Branch Tel: 0044 1202 763942 uk.sales@gema.eu.com
Wagner Spraytech (UK) Ltd.
Tel. 01327 368410
enquiries@wagner-group.com www.wagner-group.com
PARTS & PAINT SPRAY GUN WASHERS
S l t & Water Solvent W t Washers W h Manual | Automatic
www.solutex.co.uk e: info@solutex.co.uk info@solutex co uk t: 01691 622 225
69
MATERIAL & EQUIPMENT SUPPLIERS SOLVENT RECYCLING
SPRAY BOOTHS
SOFTWARE
ULTRASONIC
Final Cleaning • Spray Wash In-process Cleaning Aqueous Ultrasonics Precision Cleaning • FPI Lines Degreasing • Anodising Chemical Cleaning for MRO Chemical Etching/Milling E sales@turbex.co.uk T 01420 544 909 F 01420 542 264
SPRAY WASH
turbex.co.uk POWDER
Shyre Final Cleaning • Spray Wash In-process Cleaning Aqueous Ultrasonics Precision Cleaning • FPI Lines Degreasing • Anodising Chemical Cleaning for MRO Chemical Etching/Milling
THERMAL FLUID
E sales@turbex.co.uk T 01420 544 909 F 01420 542 264
www.unitechshyre.co.uk 01543 224531 info@unitechshyre.co.uk
turbex.co.uk
Thermal Fluid Heating
Equipment +Chemistry + Support =
Total Cleaning Solutions
Technology now for the future
✓ Over 50 years expertise ✓ New generation chemistries & equipment ✓ Superior performance & results ✓ FREE audit & trial facilities ✓ Extremely eco-friendly, safe and reliable
• • • • • • • • •
Up to 50% energy savings Compact size Easy & safe to use Works up to 350°C Low exhaust emissions High efficiency Requires no specialist knowledge Corrosion free operation No chemical treatment
Tel: 020 8953 7111
info@babcock-wanson.com www.babcock-wanson.com
01506 443058 www.frasertech.co.uk
VIBRATORY DEBURRING, POLISHING & SURFACE FINISHING
• PLANT CONTROL SYSTEMS • DATA MANAGEMENT SYSTEMS • BARRELS - PROGALVANO ROTOR • BARREL AUTO LOADING SYSTEMS • PROGALVANO FILTERS • SEMI/AUTOMATIC FILTER SYSTEMS • CENTRIFUGAL DRYERS (Large Range) • AUTOMATIC DRYING SYSTEMS • ROTARY PAINTING/LAQUERING • TOP COATING/SEALING SYSTEMS • VIBRATORY POLISHING EQUIPMENT • LUBRICATION EQUIPMENT • RECTIFIERS Conventional & Pulse • A/HOUR METERS & DOSING PUMPS
70
Precision Cleaning Specialists
VIBRATORY FINISHING EQUIPMENT & MATERIALS
FOR ALL YOUR VIBRATORY FINISHING EQUIPMENT AND MATERIALS
SHARMIC FOR FAST, FRIENDLY SERVICE
Shyre Precision Cleaning Specialists Unitech Shyre we’re leading in developing and delivering specialised cleaning processes and equipment to the precision optical industry.
Cleaning is a manufacturing process, not an afterthought. MACHINE, PROCESS, CHEMISTRY SYNERGY BY DESIGN, MADE IN THE UK, SUPPORTED WORLDWIDE www.unitechshyre.co.uk | 01543 224531 | info@unitechshyre.co.uk
WASHING SYSTEMS
WASHING SYSTEMS
New Product Alert!!
Experienced Engineers After sales technical support Nationwide deliveries
Sharmic Engineering Ltd Telephone: +44 (0)1299 822135 or +44 (0) 1299 878123/4/5 Email: info@sharmic.co.uk www.sharmic.co.uk
Cabinet Parts Washer Tel:01543 224608 | Email washers@unitech.uk.com
PosiTector Inspection ®
D
D
es
Unrivaled probe interchangeability for all of your inspection needs.
ig
es
ig
N
E N a n E nd W an W F d e n
Coating Thickness Probes n Ferrous n Non-Ferrous n Combination n Ultrasonic
Surface Profile Probes
Fe
at
ur
at
es
n Depth Micrometer n Replica Tape Reader
Environmental Conditions Probes n Integral n Cabled Magnetic Probe n Anemometer Probe n 1/2” NPT n Infrared
Hardness Probes n Shore n Barcol
Salt Contamination Probe n Bresle Method
Ultrasonic Wall Thickness Probes n Corrosion n Multiple Echo Thru-Paint n Precision n Low Frequency n Xtreme
Customized Inspection Kits... Build your own kit from a selection of gauge bodies and probes to suit your needs. Coating Thickness
Surface Profile
Environmental Conditions
Hardness
Salt Ultrasonic Contamination Wall Thickness
Backwards Compatibility! The redesigned PosiTector gauge body accepts ALL coating thickness (6000/200), environmental (DPM), surface profile (SPG/RTR), salt contamination (SST), hardness (SHD/BHI), and ultrasonic wall thickness (UTG) probes manufactured since 2012.
DFT DFTInstruments InstrumentsUK UKLTD LTD
16A Long Drive, Meadway, Berkhamsted, Herts HP4 2PN 16A Long Drive, Meadway, Berkhamsted, Herts HP4 2PN t: t: 01442 879494 f: 01442 879595 01442 879494 f: 01442 879595 www.dftinstruments.co.uk sales@dftinstruments.co.uk www.dftinstruments.co.uk e:e: sales@dftinstruments.co.uk Proud supplier ofof DeFelsko Inspection Instruments Proud supplier DeFelsko Inspection Instruments
ur
es
PUT QUALITY ON REPEAT Let‘s talk about powder coating. A technology that is proven since decades and actually, it‘s just getting started with FLOWSENSE. FLOWSENSE? It‘s a software masterpiece and a bunch of small sensors that do big things: Consistent powder output from the first to the last workpiece. Reliability, measured in real time. Put quality on repeat!
go.wagner-group.com/flowsense
Contact Wagner Spraytech (UK) Ltd Telephone: 01327 368410 enquiries@wagner-group.com